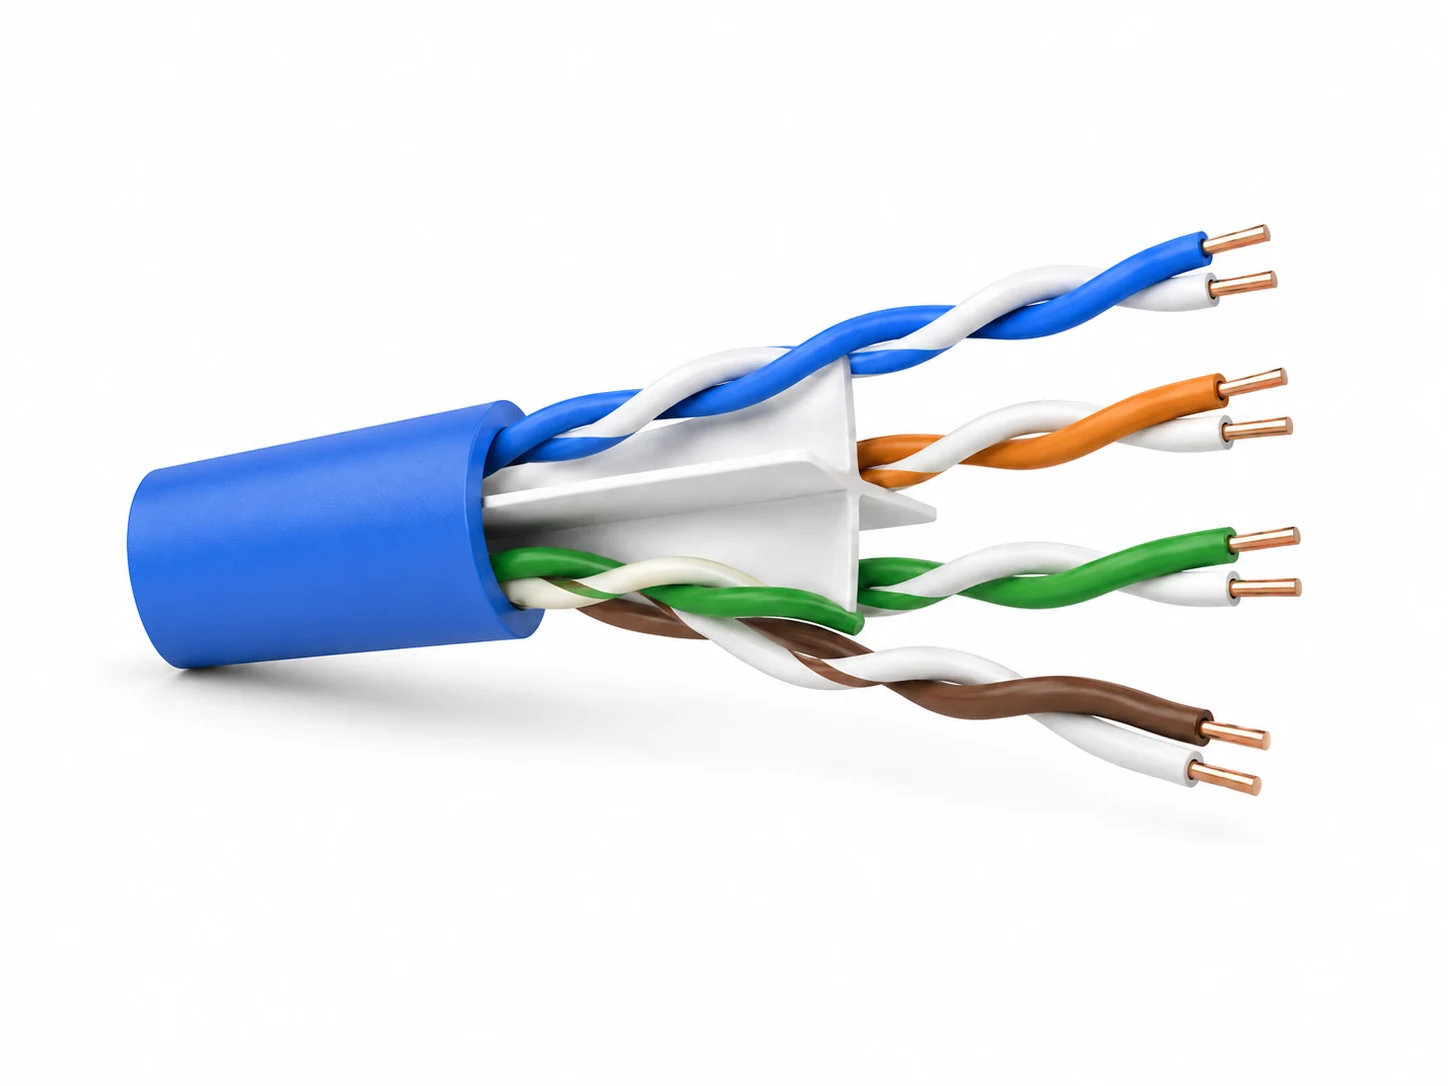
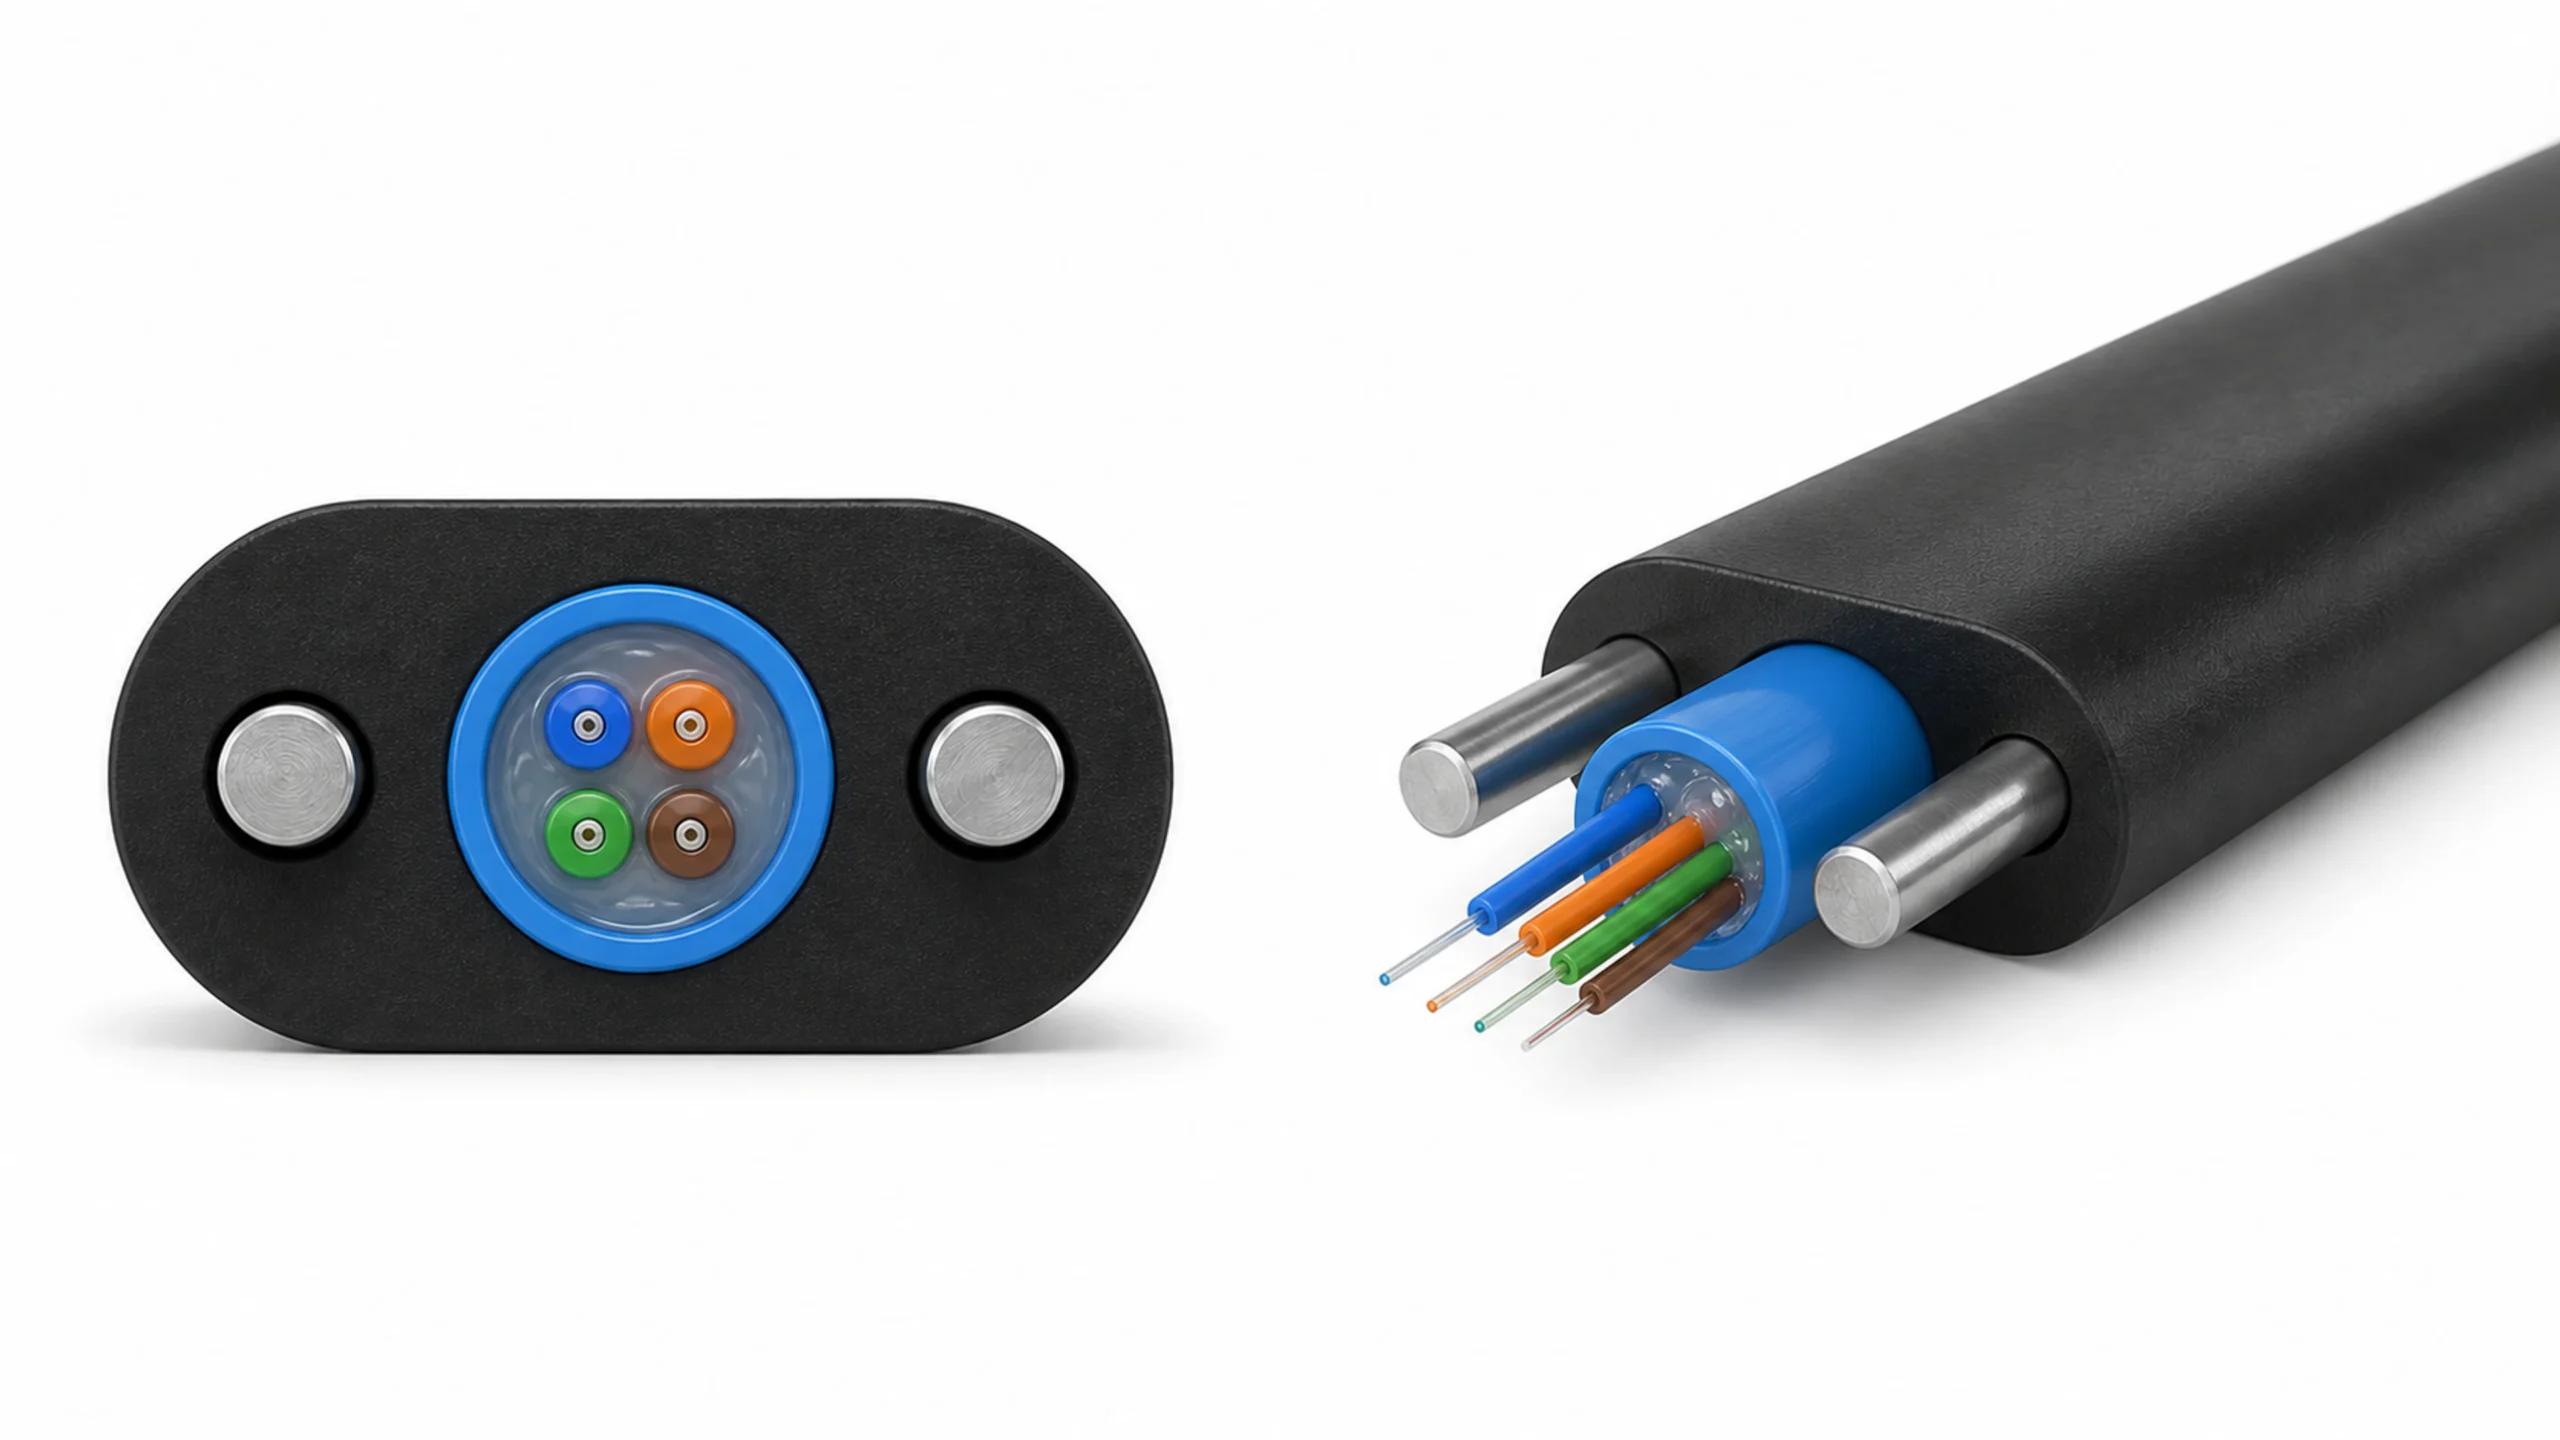
Coordinate melt delivery, tooling, cooling and traction around the cable design.
제품 및 생산
제작하려는 케이블부터 시작하세요.
HONGKAI 기계 장비의 교체 부품.
공장을 완전히 계획하고 계십니까?
제품, 생산 라인 및 자재 요구사항을 연결하세요.
Φ90 mm 압출 · 코어 공급부터 완제품 케이블 권취까지
USD 118,900 per set
Quoted configuration: HK-90 PLC+IPC Control Outdoor Optical Cable Sheathing Production Line. Ex-factory delivery; the buyer arranges and pays transport. Final equipment and tooling follow the agreed configuration schedule.
Apply the specified outer sheath around your prepared optical cable core. Configure material feeding, aramid yarn stranding or metal-tape protection as required, extrusion, cooling and take-up as one coordinated production stage.

Coordinate melt delivery, tooling, cooling and traction around the cable design.
Scope boundary: this page covers the sheathing stage. Upstream coloring, loose-tube extrusion and SZ core stranding are separate processes. Reinforcement and armoring modules are selected for the approved cable construction.
Build the process around the cable layers. Optional protection modules are selected before the extrusion and downstream handling requirements are finalized.
Start with the prepared core or loose tube. Match the core, wire and protection-material pay-offs to the incoming package.
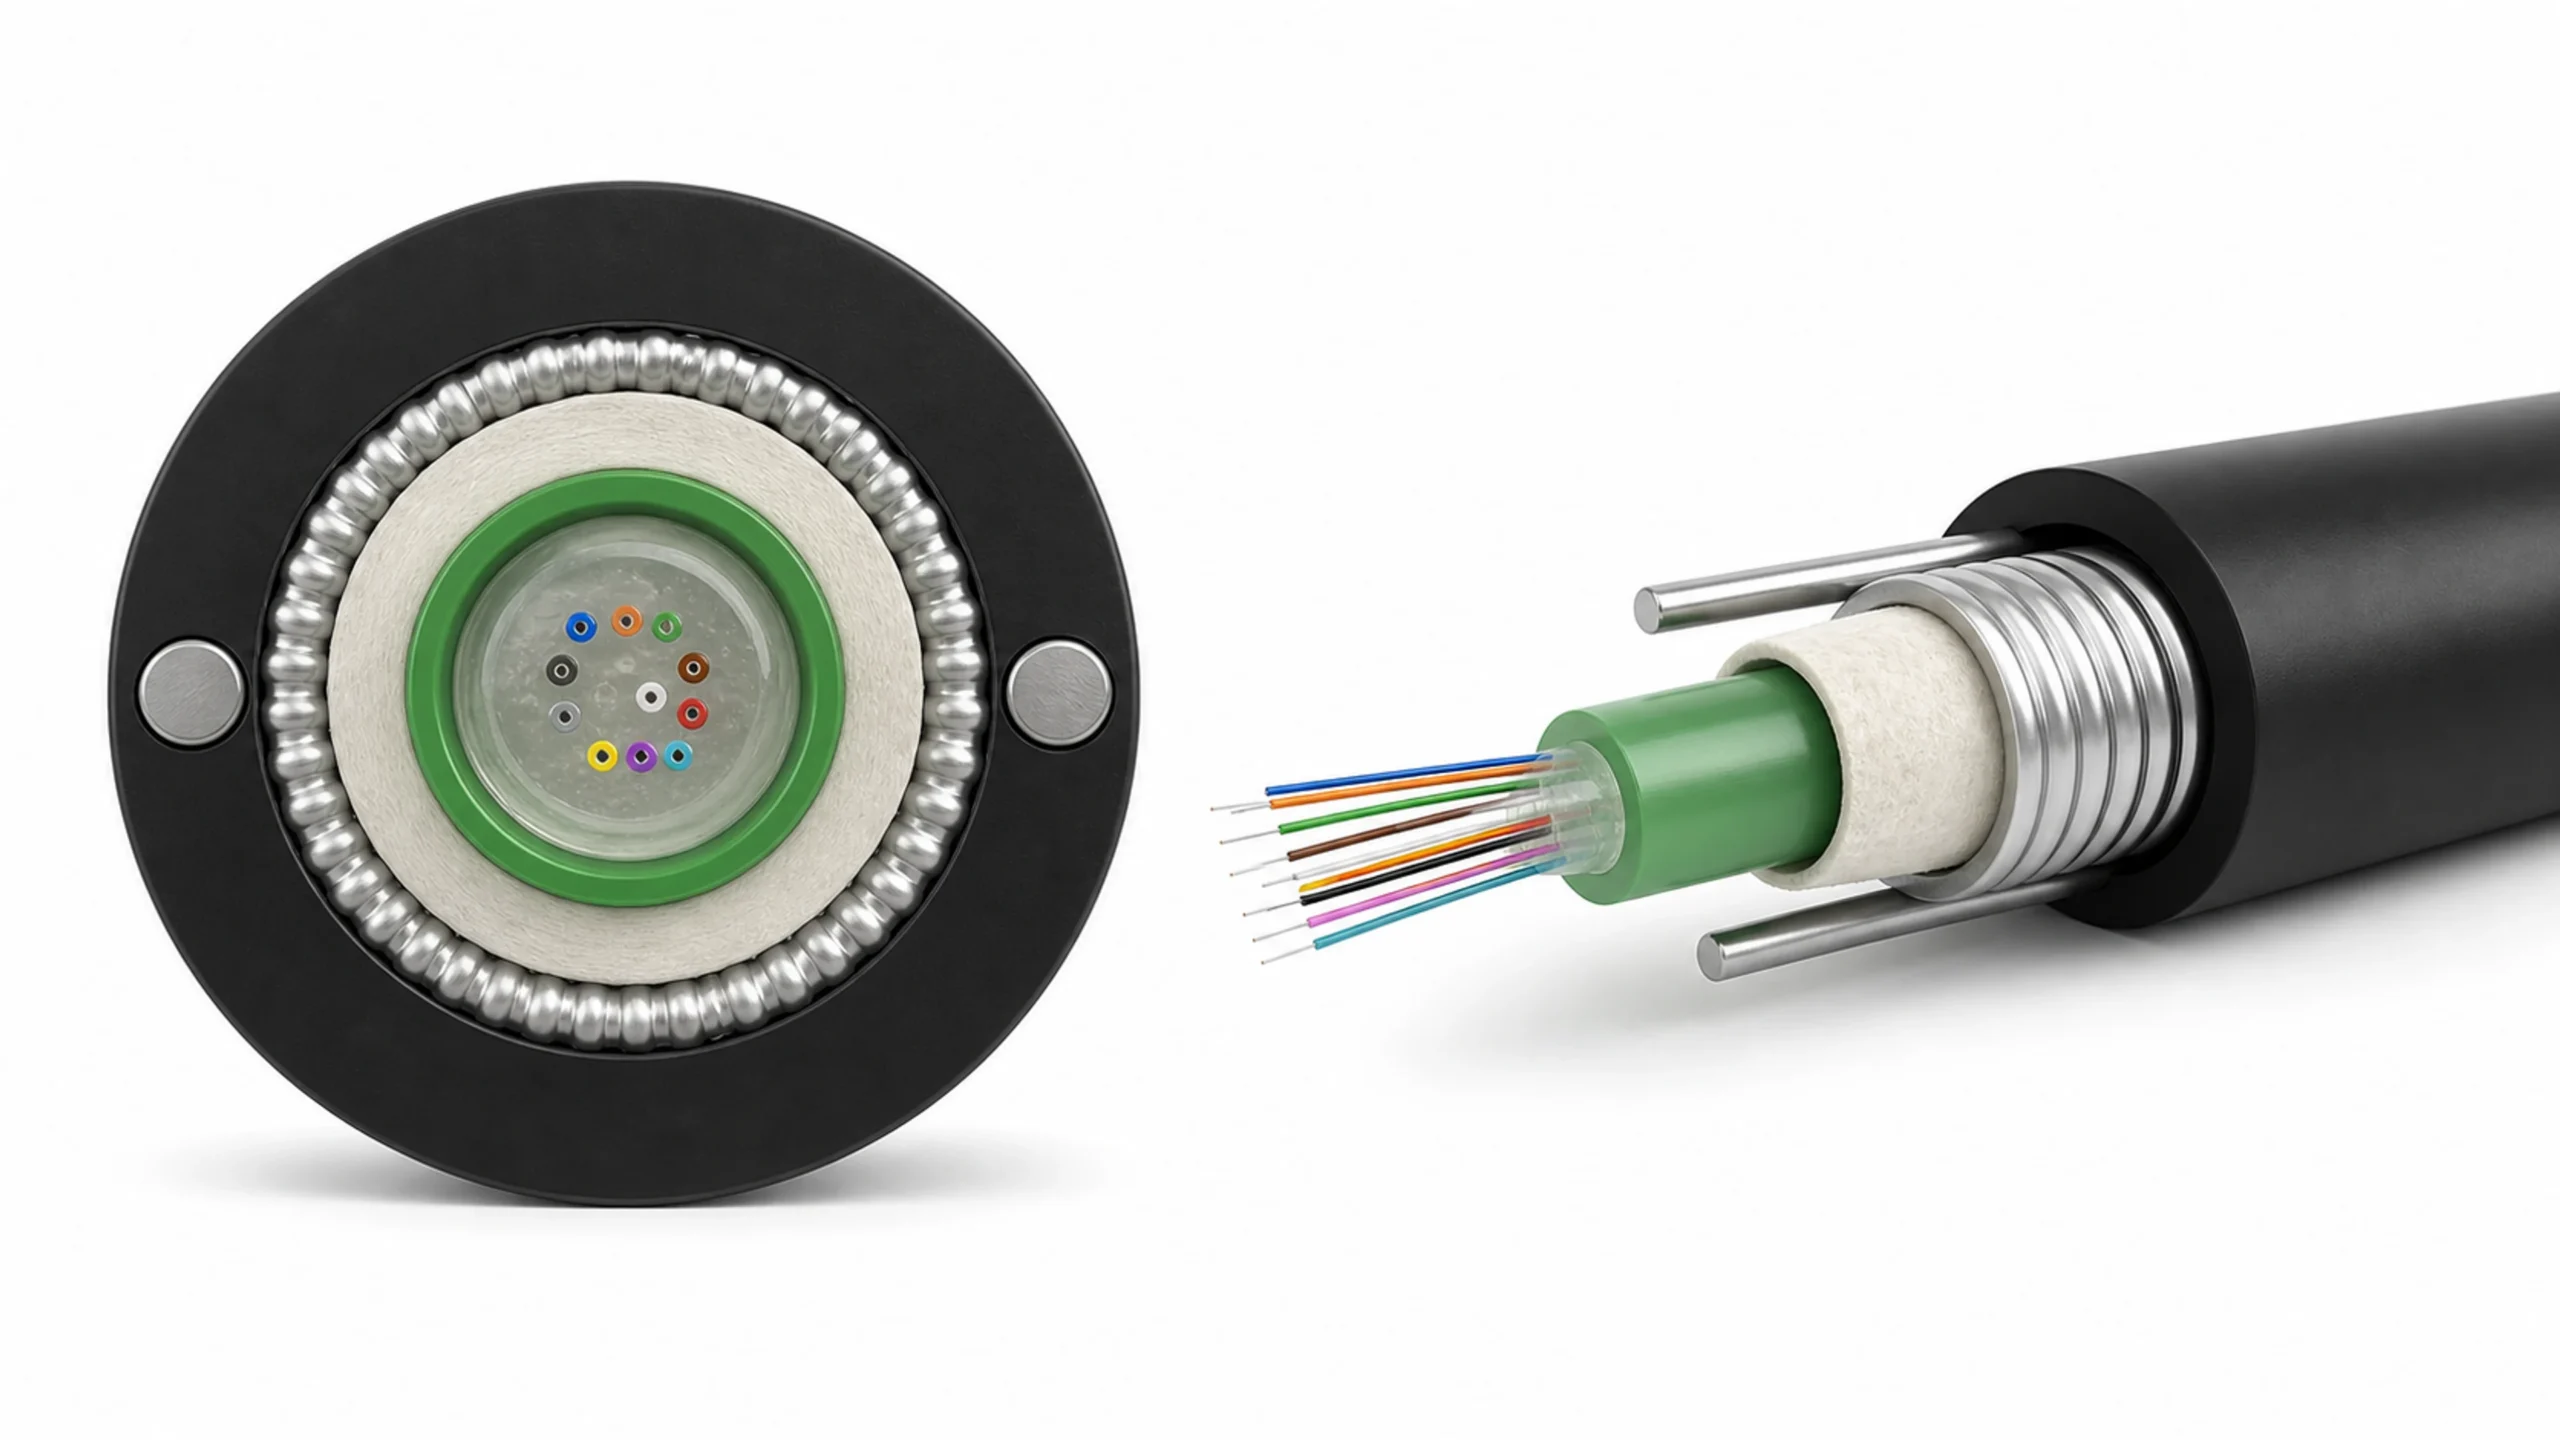
Apply the selected water blocking and ripcord. ADSS routes add aramid yarn stranding before the outer sheath; armored routes use the specified metal-tape preparation and forming modules.
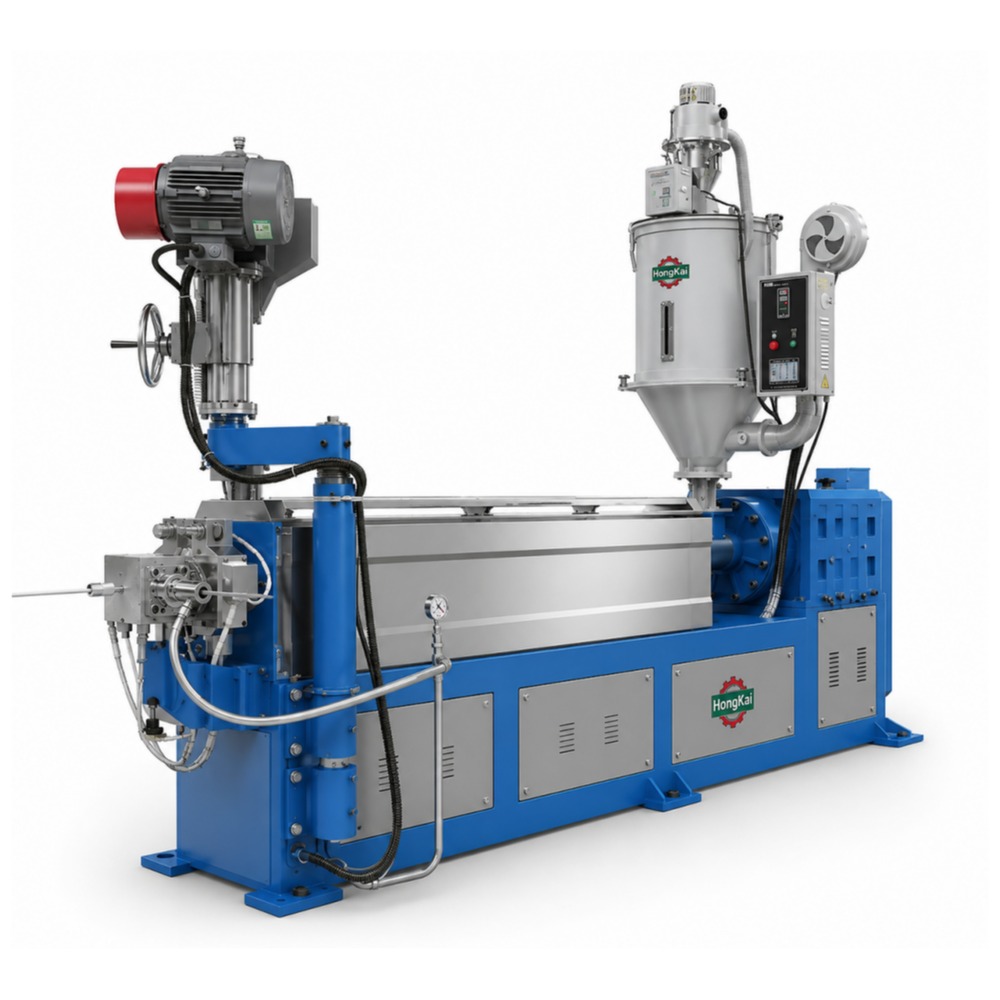
Feed the approved compound to the Φ90 mm extruder and crosshead. Coordinate melt delivery, cable centering, temperature and line speed.
Cool and dry the sheath, monitor diameter, apply the specified marking and tests, then coordinate caterpillar traction with finished-cable take-up.
Rotate the HK-90 line, select a device for a closer look, and compare its exterior with the original equipment photograph.
Preparing the interactive line…
The interactive view could not finish loading. Retry the 3D view, or use the equipment references on this page.
Illustrative exterior study. Final equipment, dimensions and layout follow the approved project configuration.
The same extrusion stage can sit within different process routes. Compare the incoming core, reinforcement and tape requirements before defining the equipment package.
Select a number or equipment card to see its equipment area, image and process role. Dashed regions identify process interfaces whose final position must be confirmed. The reference includes optional preparation and testing modules; the final equipment list follows your cable construction.
13 · Φ90 mm sheath extruderEquipment area in the reference arrangement

Equipment shown is for reference. Final construction and quantity follow your approved equipment list.
Plasticizes the approved sheath compound and supplies the adjustable crosshead. The reference uses a Φ90 mm screw with a 25:1 L/D ratio.
Compound grade, screw and crosshead, tooling, temperature profile, output and required jacket dimensions.
Selected equipment 13: Φ90 mm sheath extruder
참조 경계: the panorama illustrates equipment order, not the final machine count, footprint or construction. The approved layout and equipment list define machine quantities, dimensions and the supplied arrangement.
아래의 참조 자료를 사용하여 기술 검토를 시작하십시오. 생산 성능에 동의하기 전에 완전한 케이블 구조, 재질 등급 및 시험 조건을 확인하십시오.
| Review area | Reference / requirement | 확인할 조건 |
|---|---|---|
| Extruder reference | Φ90 mm screw · 25:1 L/D · 75 kW main drive. | Reference equipment configuration; screw, crosshead and tooling must suit the compound and cable. |
| Aramid stranding reference | 24 heads · independent tension · adjustable pitch · S or Z lay. | Selected for the cable construction. Confirm yarn grade, quantity, tension and stranding pitch together with extrusion speed. The reference 120 rpm rotation is not a cable line speed. |
| Sheath materials | PE / PVC for the reference extruder configuration. | Confirm the compound grade and process settings. Other compounds require a separate suitability review. |
| 생산 속도 | Reference: up to 80 m/min for PE cable below Φ10 mm. | Reference value; confirm the complete construction, jacket thickness, cooling, reel changes and quality targets. |
| Extrusion output | Reference: up to 250 kg/h PE, with the crosshead open. | An extruder-output reference is not guaranteed finished-cable throughput. Verify it with the agreed tooling and compound. |
| Cable & tooling range | Specify incoming core, finished diameter and jacket thickness. | Review every module. A metal-tape forming tool may have a narrower range than the extruder or capstan. |
| Reels, tension & utilities | Agree supply/output drums, winding tension, layout and utility loads. | Use one approved schedule for the chosen configuration; do not infer these values from the HK-90 name. |
| Controls & acceptance | PLC / IPC coordination, recipes, alarms and agreed inspection records. | Define instruments, interfaces, safety functions, trial duration and acceptance criteria. |
Review output together with the sheath cross-section, compound, tooling and cooling capacity. Reel capacity, line footprint, tension settings and utility loads are finalized for the selected configuration.
Compare the complete cable route, then define the sheathing equipment and construction-specific preparation modules.

Review the loose-tube input, parallel strength members, metal-tape protection and outer-sheath requirements.
Open cable solution
Coordinate aramid yarn stranding with outer-sheath extrusion; confirm whether the incoming cable is a prepared core or an inner-sheathed cable.
Open cable solution
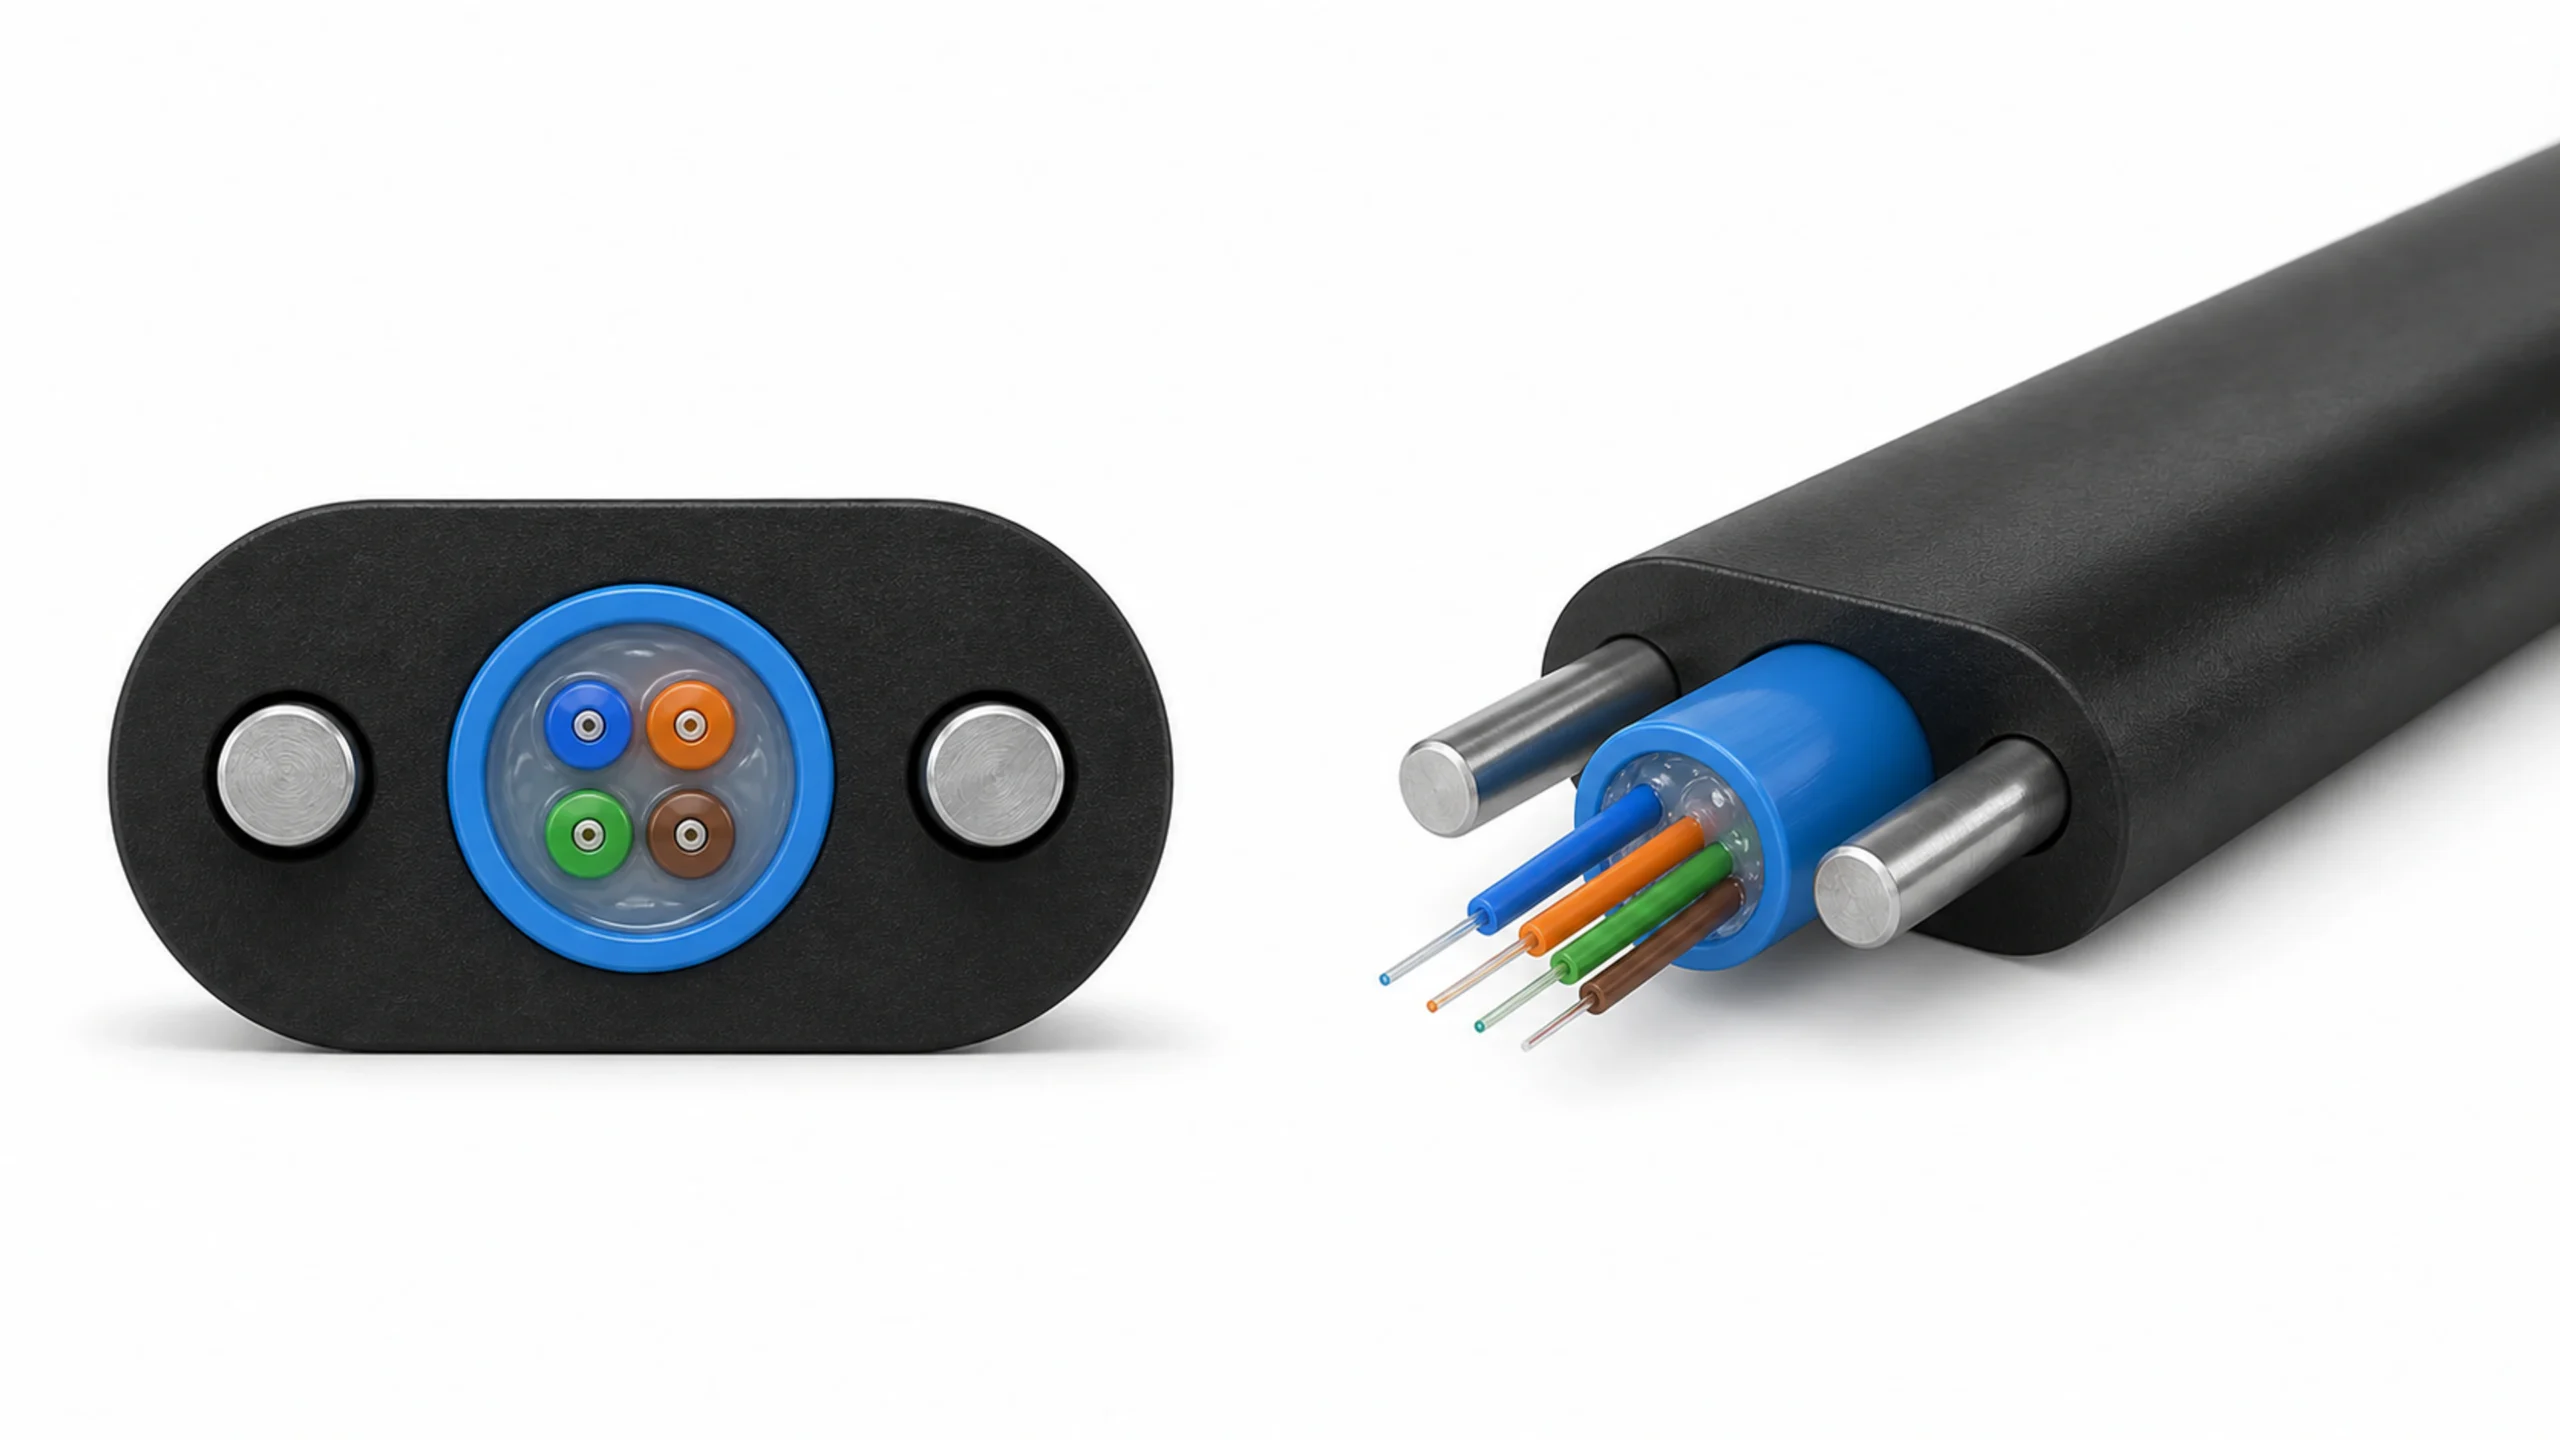
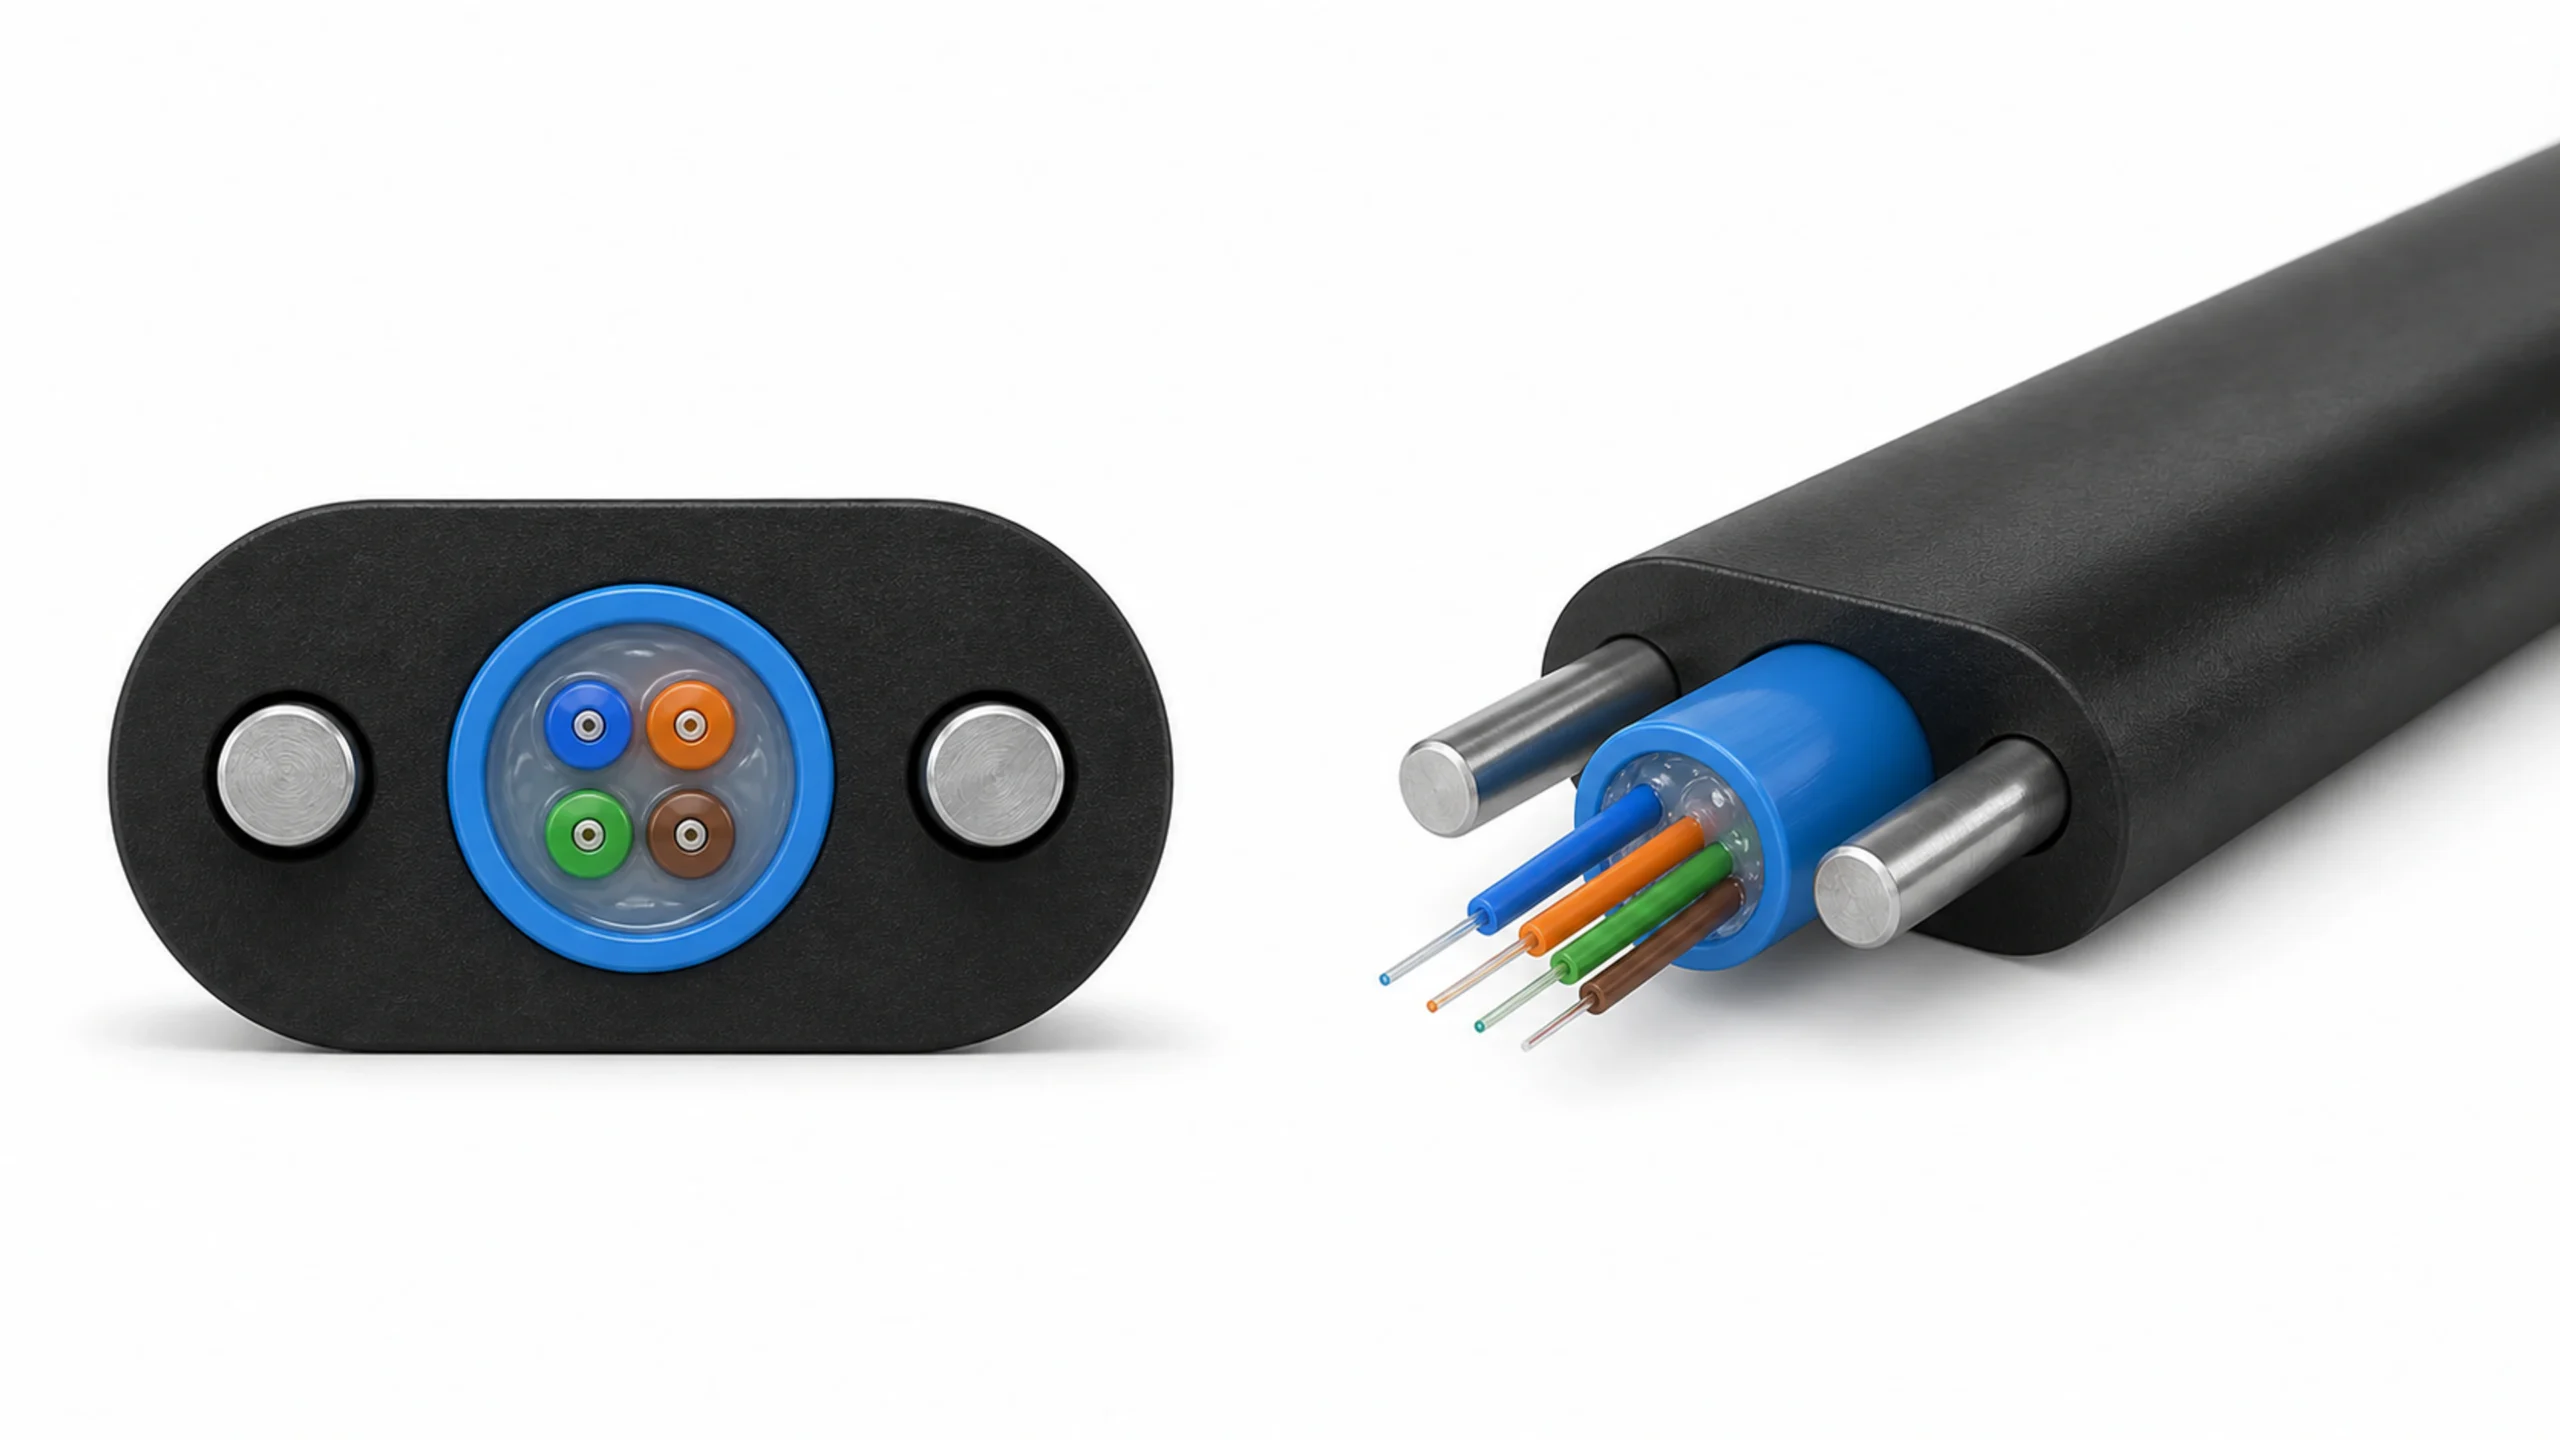
Review the published construction, armoring, messenger positioning and figure-8 crosshead tooling together.
Open cable solutionConstruction matters: armored, all-dielectric and figure-8 cables require different preparation, reinforcement and tooling. One illustrated arrangement does not establish compatibility with every cable.
For tube extrusion, review the 느슨한 튜브 생산 라인. 꼬임 심선의 경우, 다음을 검토하세요. SZ 연합 와이어 생산 라인.
The HONGKAI HK-90 video shows a sheathing reference for an ADSS cable route. Use it to discuss equipment and operating sequence, then agree the trial for your construction.
Use the approved core, sheath compound, protection materials and output drum.
Observe extrusion, cooling, diameter monitoring, traction and take-up during starts, steady running and stops.
Check finished diameter, sheath thickness and appearance, marking, winding and the agreed optical and jacket tests.
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
귀하의 도면, 제품 요구사항 또는 기존 장비부터 시작하십시오. 기술적 세부사항은 첫 번째 검토 시 확인할 수 있습니다.
Cable drawing and finished dimensions
Incoming core or loose-tube details
Sheath compound and jacket thickness
Reinforcement, tape and ripcord requirements
Input and output drum sizes / weights
Target output and operating plan
Marking, testing and acceptance criteria
Factory layout and retained equipment
Utilities, installation and project timing
Review the cable construction, equipment boundary and information needed for a proposal.
해당 공정은 준비된 광케이블 코어 또는 구조별 튜브 및 보호 패키지에 지정된 외피를 적용한 후, 케이블을 냉각하고 검사하여 권취한다. 상류 공정인 광섬유 컬러링, 로스튜브 압출 및 SZ 연선은 별도의 단계로 간주되며, 프로젝트 범위에 포함되지 않는 한 본 공정에 포함되지 않는다.
이 케이블 계열에는 HK-90 피복 공정이 포함될 수 있지만, 동일한 장비 패키지를 사용하지는 않는다. 각 케이블 도면에 대해 코어 처리, 보강재, 아머링, 메신저 와이어 위치 설정, 크로스헤드 툴링 및 하류 시험을 검토해야 한다.
금속 테이프의 방출, 접합, 축적, 주름 형성 및 종방향 성형은 지정된 피복 또는 복합 외피 구조를 위해 선택됩니다. 전유전체(All-dielectric) 경로는 다른 보강 요건을 갖습니다.
The reference ratings are up to 80 m/min for PE cable below 10 mm and an extrusion-output reference of up to 250 kg/h PE with the crosshead open. These values describe stated reference conditions. Actual accepted cable output must be agreed for the cable, compound, tooling, cooling and operating plan.
The supplied extruder reference describes PE and PVC. Confirm the exact grade and required screw, tooling, drying and temperature settings. Do not assume that LSZH or another compound is covered without a separate engineering review.
장비 사양에는 테이프 접합 공정을 위해 테이프를 저장하는 금속 테이프 애큐뮬레이터가 포함됩니다. 완성 케이블 애큐뮬레이터는 다른 역할을 수행하므로 자체 구성, 장력, 저장 길이 및 릴 교체 점검이 필요합니다.
시험 적용성은 케이블 구조와 적절한 전기적 복귀 경로에 따라 달라진다. 유전체만으로 구성된 케이블에는 금속을 포함한 케이블과 동일한 스파크 시험 장치를 자동으로 적용해서는 안 된다. 실제 제품에 대한 시험 방법 및 합격 기준을 확인하라.
케이블 도면, 인입 코어, 시스(외피) 컴파운드, 보호재, 필요한 드럼 사이즈 및 생산 목표를 보내주십시오. 가능하면 공장 레이아웃과 기존 장비도 함께 제출해 주세요. 기술적 세부사항은 첫 번째 검토 단계에서 완료할 수 있습니다.