






An indoor optical-cable line should not be quoted as an outdoor line simply because its extruder can process PE. For the HONGKAI routes discussed here, the cable structure determines the production scope. Buyers need a construction-specific proposal, not a material-change shortcut.
A screw suitable for the specified PVC and PE compounds does not make a complete indoor and outdoor fiber cable line interchangeable. Define the cable construction first, then specify its protection, core-forming, sheathing, output and inspection requirements.
This comparison separates three decisions: the material scope of an extrusion component, the complete route required by a cable product, and the sheathing arrangement selected for that product. It is a guide to defining equipment scope, not a claim that an existing indoor line can be converted into an outdoor line.
장비 경로보다 시공을 먼저 선택하세요
Indoor and outdoor identify intended environments, not complete cable drawings. Record the target product’s actual fiber protection, core arrangement, reinforcement, water-management provisions and sheath package before comparing equipment. A familiar product label is not enough to define the manufacturing route.
코닝의 실내/실외 적용 가이드라인에는 자체 제품군 내의 틱트 버퍼드, 루즈 튜브 및 리본 구조가 포함됩니다.1 That prevents a rigid indoor-equals-tight-buffer and outdoor-equals-loose-tube rule. It does not establish that an unspecified HONGKAI line can make those products or deliver the same qualifications.

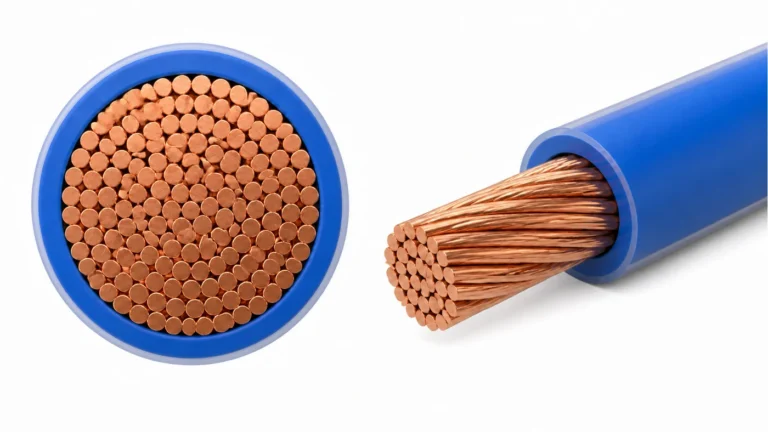
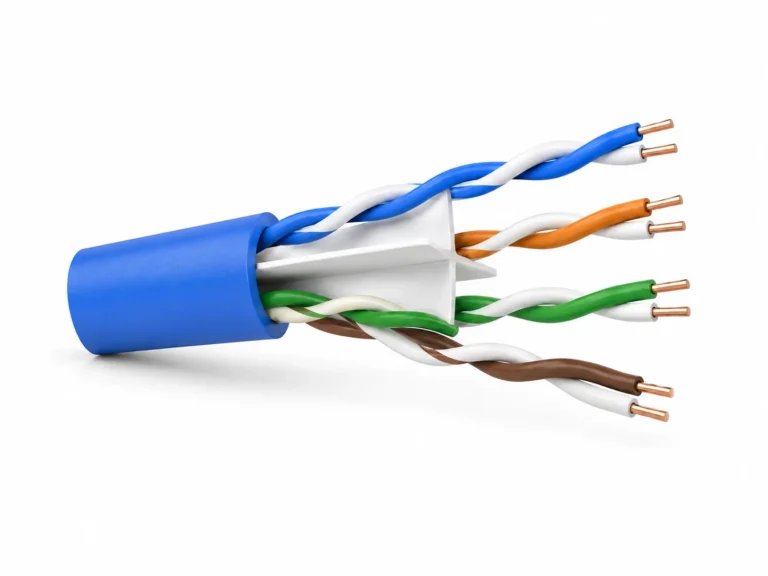
Conceptual component illustrations, not complete cable designs or dimensions. Tight buffering and loose-tube protection are separate construction choices; neither alone defines an indoor or outdoor product.
Use the following comparison to identify the two product scopes. Complete both columns from the intended products, rather than filling the outdoor column with assumptions about what an indoor line might be modified to make.
| Construction boundary | 지정된 실내용 제품 | 지정된 야외용 제품 |
|---|---|---|
| 광섬유 입력 | 광섬유 사양, 코팅 또는 버퍼 상태 및 공급 패키지 | 필요한 섬유 사양 및 각 공정 입력 양식 |
| 섬유 보호 | 지정된 조밀 버퍼, 튜브 또는 기타 보호재 및 그 치수 | 지정된 보호 구조, 재질 및 치수 |
| 케이블 코어 조립 | 소자 배치 및 요구 강도 구성 요소 | 튜브 또는 서브유닛 배열, 보강 및 필요한 코어 형성 방법 |
| 물 관리 기능 | 명시된 재료 및 해당 요구 기능 | 관 및 케이블 코어 요구사항, 실제 위치로 할당 |
| Sheath package | Compound 등급, 층 수, 유입 요소 및 완성된 형상 | 각 층의 화합물, 형상 및 중간 제품 |
| 제품 자격 및 취급 | 목표 요구사항, 테스트 범위 및 완제품 패키지 | 목표 요구사항, 테스트 범위 및 완제품 패키지 |
For the HONGKAI indoor and outdoor routes described in this comparison, the starting point is a customized product-specific configuration. The proposed outdoor route must be defined from its own construction; it is not accepted as a conversion of the indoor route on the strength of a shared screw.
실내 및 실외 배선로가 수행하는 역할은 다릅니다
Tight buffering, loose-tube formation, cable-core assembly and final sheathing produce different intermediate or finished outputs. Their equipment duties are not interchangeable simply because several operations use extrusion. The important distinction is what enters an operation, what leaves it and which structure that output belongs to.

Conceptual process outputs, not a compulsory three-stage route. Each row illustrates a separate duty; the target construction and purchased-intermediate boundary determine which operations are required.
그만큼 HONGKAI HK-30 tight-buffered-fiber reference describes a fiber-protection duty with fiber handling, buffer extrusion and downstream equipment. Its output is tight-buffered optical fiber, not automatically a complete indoor multi-fiber cable. The rest of the product’s assembly and sheathing scope must still be identified.
그만큼 루즈튜브 생산 라인 참조 addresses a different intermediate: fibers contained in the specified tube. The described outdoor loose-tube options can involve gel-filled or non-gel arrangements. A central-tube product and a stranded-tube product can also require different downstream core-forming operations; an SZ stage is not added to every outdoor design by default.
Fiber Optic Association는 광섬유 보호, 강도 보강재, 재킷 및 차수 조치를 별도의 구조 기능으로 구분합니다.2 이러한 기능들은 적절한 압출 스크류가 생산 공정의 나머지 부분을 어떻게 확립하지 못하는지를 설명하는 데 도움이 됩니다.
Water management must be specified separately from tube dimensional control. HONGKAI’s earlier description of a vacuum-assisted, non-gel optical-tube operation concerns diameter stabilization; it is not evidence of longitudinal water-blocking performance. The 젤 충전형과 건식 코어 광케이블 비교 다양한 선택 작업을 커버합니다. 여기서 구매자는 각 단계에서 필요한 기능, 소재 및 장비 책임을 식별해야 합니다.
Also state whether protected elements or prepared cores will be made in-house or purchased. A project starting with purchased tubes does not have the same supply boundary as one starting with optical-fiber packages. Neither boundary should be hidden inside a generic promise of a complete indoor or outdoor line.
A Shared Screw Does Not Make a Convertible Line
In the PVC/PE applications described by HONGKAI, a suitably specified screw can serve both materials. That is a component-level material scope, not approval to convert an indoor optical-cable line into an outdoor line.
HONGKAI’s discussion of outdoor sheathing emphasizes PE rather than treating a change from PVC as a complete process specification. Identify the actual compound in the product brief. LDPE, MDPE and HDPE describe PE families, not interchangeable approved grades, and those examples are not an exhaustive classification of polyethylene. Original material suppliers publish different jacketing families and grades, which reinforces the need for an exact compound designation.3
For the selected extrusion duty, keep the compound’s preparation and processing information with the actual screw and head specification. Check the incoming element or prepared core, applied layer geometry, required material delivery, cooling, traction and packages as part of that duty. Do not substitute a generic temperature, drying instruction or PE label for the specified compound and product.
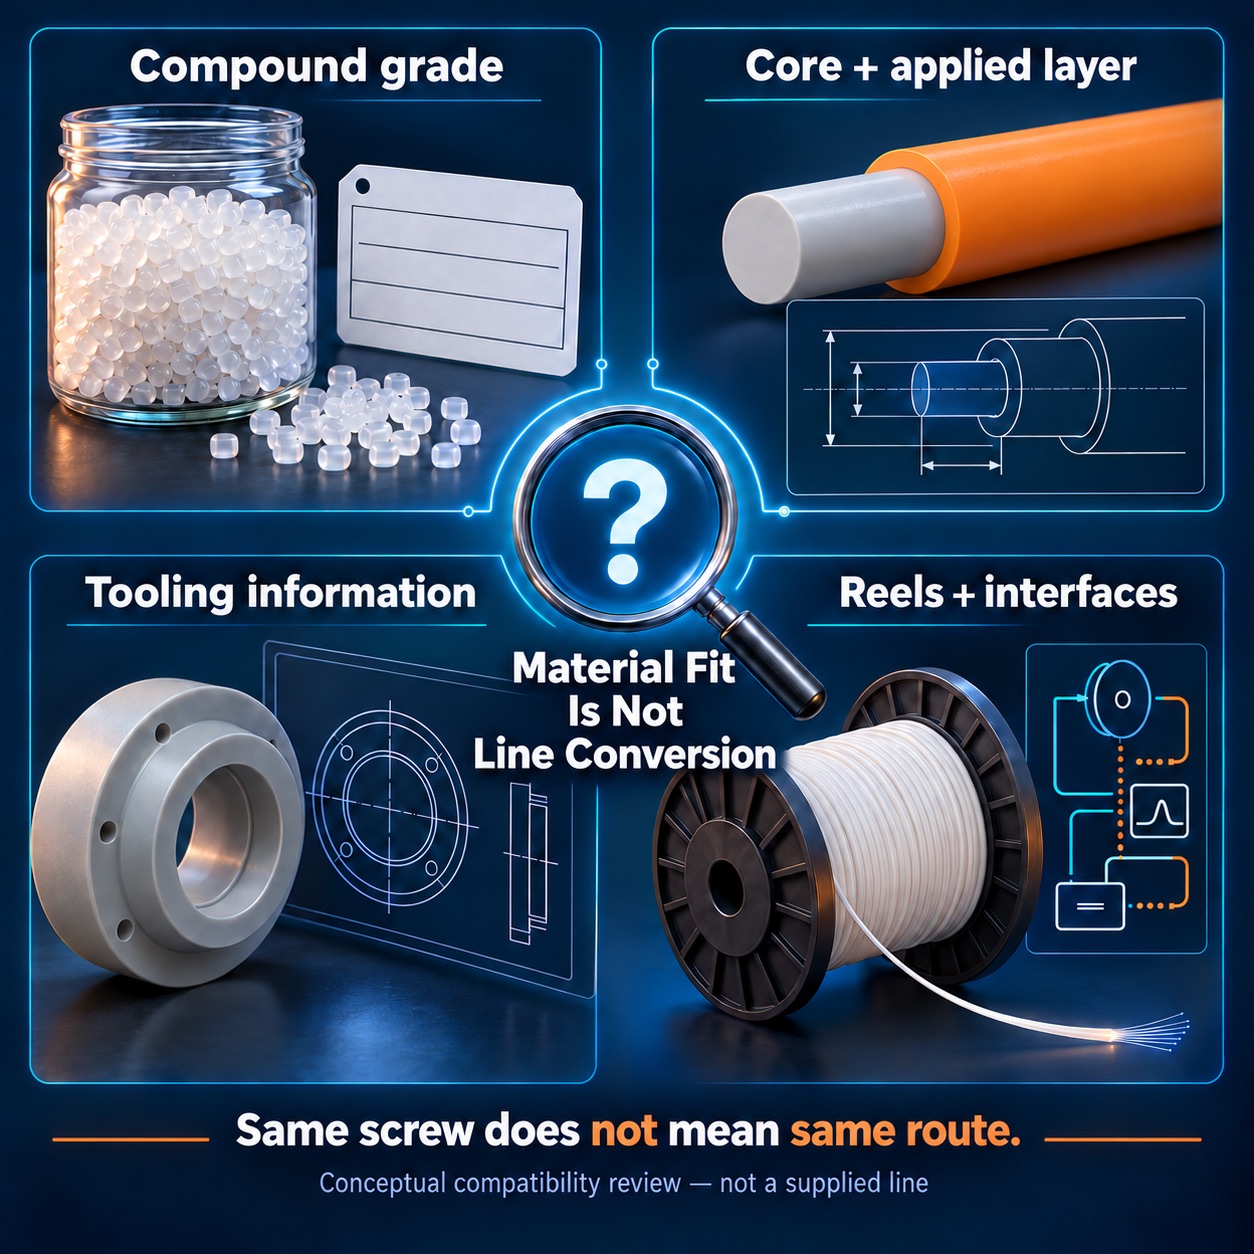
Conceptual compatibility review, not supplied equipment or a complete cable construction. A shared material-processing component does not qualify the protection, assembly, sheathing and inspection duties of a different cable route.
그만큼 HK-90 optical-cable sheathing reference starts from a prepared cable core or loose tube and specified protection materials. It illustrates a sheath-stage boundary, not a universal conversion package. Screw compatibility alone does not demonstrate the required fiber handling, tube-making, core assembly, protection-material feeds or finished-product verification.
Decision criterion: Accept a proposal against the named cable and the stated process scope. Do not treat a PVC/PE screw statement, a familiar extruder model or an unexamined equipment list as proof that an indoor route can manufacture the specified outdoor product.
Double Sheathing: One Unit in Passes or Two Main Units
A double-sheath decision concerns how the specified layers will be manufactured. HONGKAI identifies the available budget as an input when choosing between one extrusion unit used in separate passes and a proposal with two main units assigned to the layer duties. This does not create a general budget threshold or a guaranteed output difference.
With one main extruder and head, the described repeat-pass approach applies one layer, produces an intermediate package and then applies the other layer in another operation. Define the intermediate product, its reel, the next pay-off condition and the tooling required for each pass. These are parts of the manufacturing sequence, not incidental handling details.
Two main units can be proposed when the project budget and requirements support that arrangement. The quotation must still state the actual layout and handoff: two units alone do not establish whether the layers are applied continuously in a coordinated line or in separate operations. Cooling, traction, heads and control responsibilities must be specified for the chosen arrangement.

Conceptual planning, not a machine layout or complete cable design. The repeat-pass example includes intermediate handling; separate main-unit duties still need an agreed layout and handoff. Layer colors do not specify materials or performance.
Compare the alternatives using the same finished cable, order pattern and output definition. Record the operations per finished drum, material and tooling changes, handling and agreed quality checks. Do not count the same manufacturing length twice as finished output or compare proposals only by an instantaneous running-speed figure.
The choice between these sheath arrangements does not supply missing upstream operations or convert an indoor product route into an outdoor one. Two sheaths also do not, by themselves, qualify a cable for both environments; the product needs its own specification and evidence.1
제품, 출력 및 테스트 범위를 함께 명시
A useful enquiry identifies the target cable by product name or model, an actual construction drawing and the required output. These inputs allow a customized route to be defined. Without them, a broad catalogue of outdoor equipment is not a commitment that one fixed configuration covers every outdoor cable.
Write the product and process boundaries into the proposal before evaluating a complete-line claim. For a product range, identify the constructions included and the evidence required for each relevant duty; an equipment-family description is not a demonstrated product range.
| Scope item | Information to put in the proposal | Boundary to resolve before acceptance |
|---|---|---|
| 대상 케이블 | 제품/모델, 도면 개정, 광섬유 형태, 코어 구조 및 층 사양 | Which products the configuration is actually intended to manufacture |
| Material and geometry | 혼합 등급, 유입 원소 또는 코어, 층 치수 및 완성 치수 | The approved material/product combination, not a generic PVC or PE promise |
| Process handoffs | 자체 운영, 구매된 중간재 및 준비된 코어에 대한 책임 | Where the supplied route begins and ends |
| Output and sheath sequence | Required output for the named cable, repeat-pass or separately assigned duties, and package drawings | What the output figure includes and which operations and handling it depends on |
| Inspection and acceptance | 제품별 시험, 장비 범위, 샘플, 기록 및 담당 부서 | What the machinery trial proves and what requires separate finished-cable evidence |

Conceptual product-scope guide, not a delivered configuration, a whole-line conversion or a test result. Name the product and drawing, define purchased intermediates and process handoffs, agree output and sheath sequence, then assign machinery-trial and remaining product-test responsibilities. Component and process illustrations are separate examples, not one compulsory route.
Indoor and outdoor products can require different inspection plans and test equipment. Define the optical checks alongside any required water-penetration, environmental, mechanical, sheath-material or fire-performance tests. An optical result does not establish all those other properties, and one generic laboratory list should not be assumed to cover both products.
Keep the machinery trial and finished-cable qualification distinct. Agree which product will be run, the material and drawing revision, the output and dimensional observations to be recorded, and the ownership of any additional product tests and reports. No hypothetical indoor-to-outdoor conversion trial or unprovided measurement dataset is used as acceptance evidence.
Evidence to request: The named target products and drawings, a stage-by-stage equipment scope, the agreed compound and tooling information, the sheath sequence, the output basis and the product-specific inspection responsibilities.
The purchase decision is therefore not whether a PE-capable screw makes an indoor line universal. It is whether the proposed production route is defined and demonstrated for the cable the factory intends to make. Material compatibility remains one bounded part of that decision, not a substitute for the complete configuration.
-
Corning Optical Communications, Optical Fiber Cables for Indoor/Outdoor Applications, AEN097, Revision 4, describes several indoor/outdoor cable constructions and product-specific qualification. Its supplier approvals, numerical specifications and historical installation-standard references are not transferred to HONGKAI equipment. ↩ ↩
-
The Fiber Optic Association, Outside Plant Fiber Optic Cable, explains separate fiber-protection, strength-member, jacket and water-management functions. Only those construction distinctions are used here, not example dimensions, costs or installation prescriptions. ↩
-
Dow’s AXELERON GP D-0588 BK telecom cable compound identifies a low-density PE jacketing grade; Borouge’s Borstar jacketing compounds lists LLDPE, MDPE and HDPE families. These sources support material terminology and grade identification, not shared-screw compatibility or HONGKAI equipment performance. ↩
 English
 हिन्दी
 فارسی