Extrusão Φ90 mm · Desenrolamento do núcleo até o enrolamento final do cabo
USD 118,900 per set
Quoted configuration: HK-90 PLC+IPC Control Outdoor Optical Cable Sheathing Production Line. Ex-factory delivery; the buyer arranges and pays transport. Final equipment and tooling follow the agreed configuration schedule.
Apply the specified outer sheath around your prepared optical cable core. Configure material feeding, aramid yarn stranding or metal-tape protection as required, extrusion, cooling and take-up as one coordinated production stage.
Coordinate melt delivery, tooling, cooling and traction around the cable design.
REFERENCE ARRANGEMENTEquipment quantities and final layout follow the reviewed project.
Scope boundary: this page covers the sheathing stage. Upstream coloring, loose-tube extrusion and SZ core stranding are separate processes. Reinforcement and armoring modules are selected for the approved cable construction.
02PROCESS & MATERIAL HANDOFF
From prepared core to finished outer sheath.
Build the process around the cable layers. Optional protection modules are selected before the extrusion and downstream handling requirements are finalized.
01CORE & MATERIAL PAY-OFF
Feed the specified construction.
Start with the prepared core or loose tube. Match the core, wire and protection-material pay-offs to the incoming package.
02PROTECTION & FORMING
Prepare the layers before extrusion.
Apply the selected water blocking and ripcord. ADSS routes add aramid yarn stranding before the outer sheath; armored routes use the specified metal-tape preparation and forming modules.
03SHEATH EXTRUSION
Form the outer jacket.
Feed the approved compound to the Φ90 mm extruder and crosshead. Coordinate melt delivery, cable centering, temperature and line speed.
04COOLING TO TAKE-UP
Cool, inspect and collect.
Cool and dry the sheath, monitor diameter, apply the specified marking and tests, then coordinate caterpillar traction with finished-cable take-up.
3DINTERACTIVE LINE VIEW
Explore the line. Inspect each device.
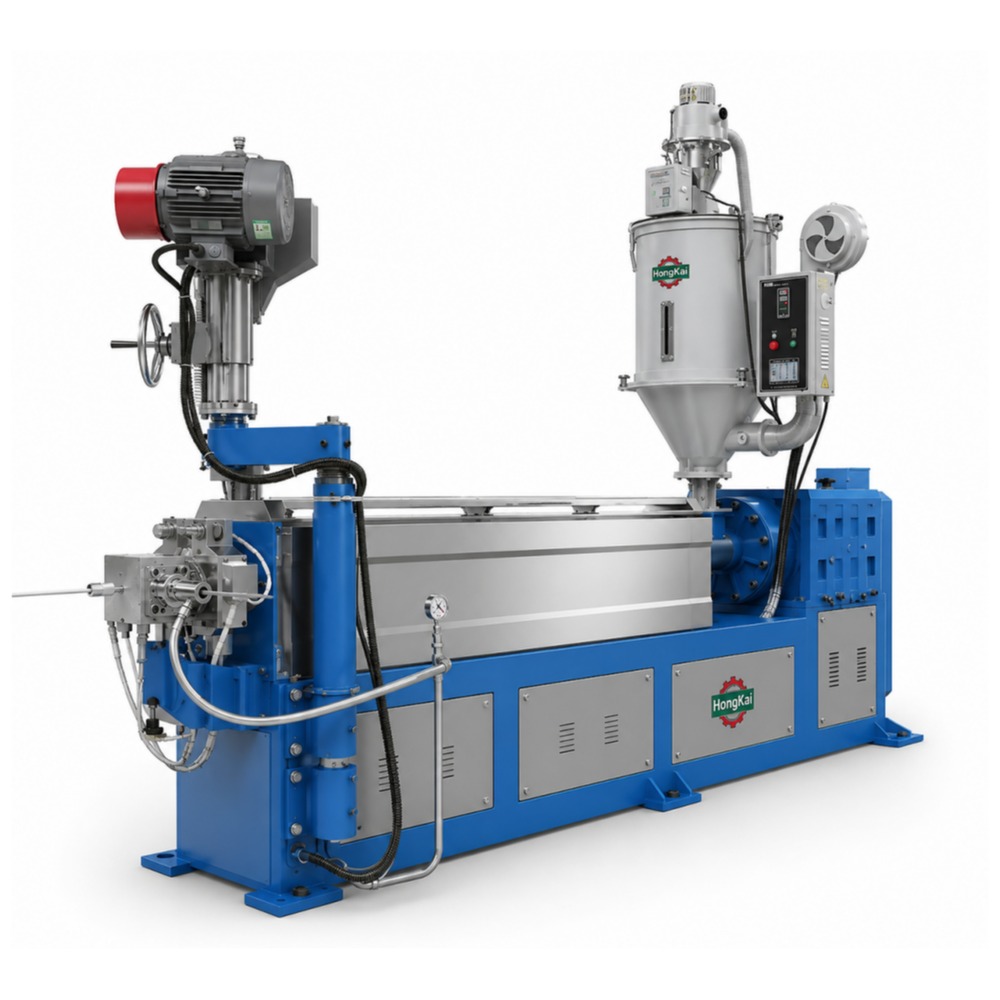
Rotate the HK-90 line, select a device for a closer look, and compare its exterior with the original equipment photograph.
Preparing the interactive line…
The interactive view could not finish loading. Retry the 3D view, or use the equipment references on this page.
Illustrative exterior study. Final equipment, dimensions and layout follow the approved project configuration.
03CONFIGURATION & PROJECT SCOPE
Choose the protection route for your cable.
The same extrusion stage can sit within different process routes. Compare the incoming core, reinforcement and tape requirements before defining the equipment package.
PROJECT EQUIPMENT REFERENCEUnidade de corrugação de fita metálica
CONFIGURATION BASISMódulos específicos de construção · escopo final por desenho do cabo
04EQUIPMENT IN THE LINE
Follow the line, one machine at a time.
Select a number or equipment card to see its equipment area, image and process role. Dashed regions identify process interfaces whose final position must be confirmed. The reference includes optional preparation and testing modules; the final equipment list follows your cable construction.
HK-90 EQUIPMENT MAP · REFERENCE ARRANGEMENT
13 · Φ90 mm sheath extruderEquipment area in the reference arrangement
SELECTED EQUIPMENT · PROJECT REFERENCE13 / 23
Equipment shown is for reference. Final construction and quantity follow your approved equipment list.
SHEATH EXTRUSION
Φ90 mm sheath extruder
Plasticizes the approved sheath compound and supplies the adjustable crosshead. The reference uses a Φ90 mm screw with a 25:1 L/D ratio.
CONFIRM FOR YOUR PROJECT
Grau do composto, rosca e cabeçote, ferramental, perfil de temperatura, produção e dimensões necessárias da cobertura.
Selected equipment 13: Φ90 mm sheath extruder
Limite de referência: the panorama illustrates equipment order, not the final machine count, footprint or construction. The approved layout and equipment list define machine quantities, dimensions and the supplied arrangement.
05TECHNICAL CONFIGURATION REVIEW
Defina as condições de operação por trás da especificação.
Use the reference below to begin the technical review. Confirm the complete cable construction, material grade and trial conditions before agreeing production performance.
HK-90 reference data and project confirmation points
Review area
Reference / requirement
Condição a confirmar
Extruder reference
Φ90 mm screw · 25:1 L/D · 75 kW main drive.
Configuração de referência do equipamento; o parafuso, a cruzeta e os moldes devem ser adequados ao composto e ao cabo.
Referência de encordoamento em aramida
24 heads · independent tension · adjustable pitch · S or Z lay.
Selected for the cable construction. Confirm yarn grade, quantity, tension and stranding pitch together with extrusion speed. The reference 120 rpm rotation is not a cable line speed.
Sheath materials
PE / PVC for the reference extruder configuration.
Confirm the compound grade and process settings. Other compounds require a separate suitability review.
Velocidade de produção
Reference: up to 80 m/min for PE cable below Φ10 mm.
Reference value; confirm the complete construction, jacket thickness, cooling, reel changes and quality targets.
Extrusion output
Reference: up to 250 kg/h PE, with the crosshead open.
An extruder-output reference is not guaranteed finished-cable throughput. Verify it with the agreed tooling and compound.
Cable & tooling range
Specify incoming core, finished diameter and jacket thickness.
Review every module. A metal-tape forming tool may have a narrower range than the extruder or capstan.
Reels, tension & utilities
Agree supply/output drums, winding tension, layout and utility loads.
Use one approved schedule for the chosen configuration; do not infer these values from the HK-90 name.
Controls & acceptance
PLC / IPC coordination, recipes, alarms and agreed inspection records.
Define instruments, interfaces, safety functions, trial duration and acceptance criteria.
CABLE DRAWING → TECHNICAL SCHEDULE → ACCEPTANCE
Confirme o cronograma técnico do seu cabo.
Review output together with the sheath cross-section, compound, tooling and cooling capacity. Reel capacity, line footprint, tension settings and utility loads are finalized for the selected configuration.
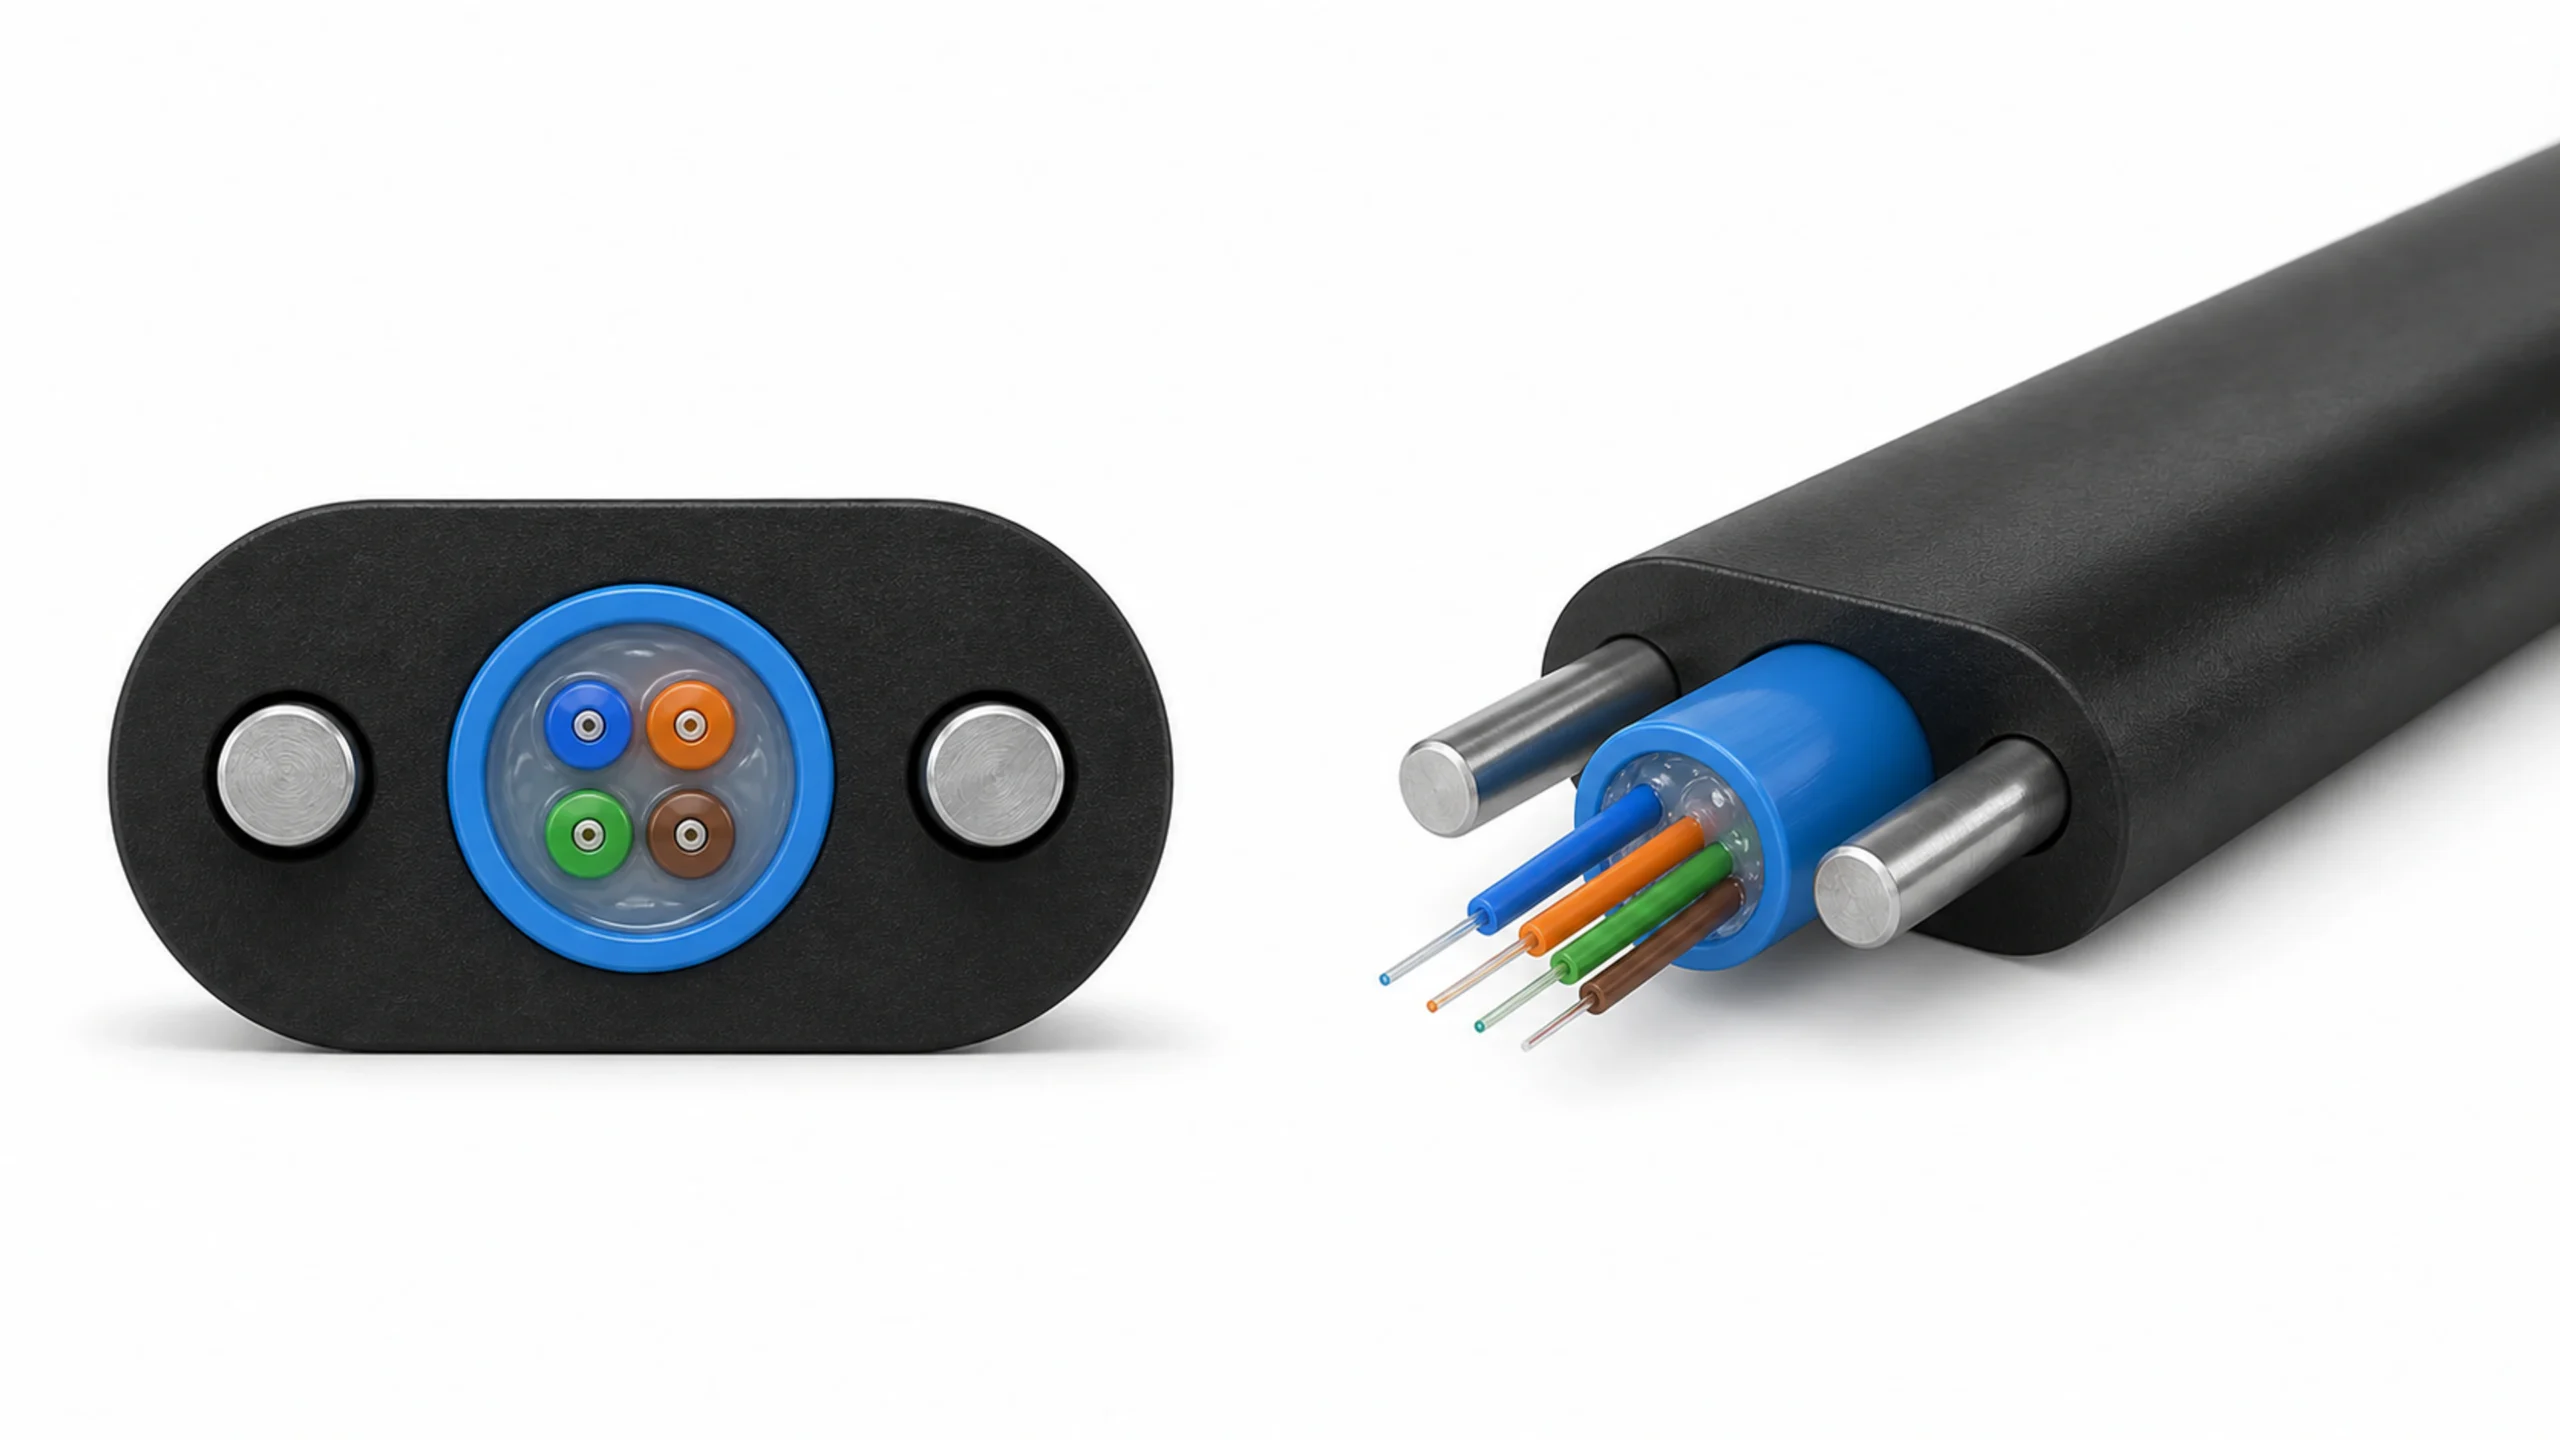
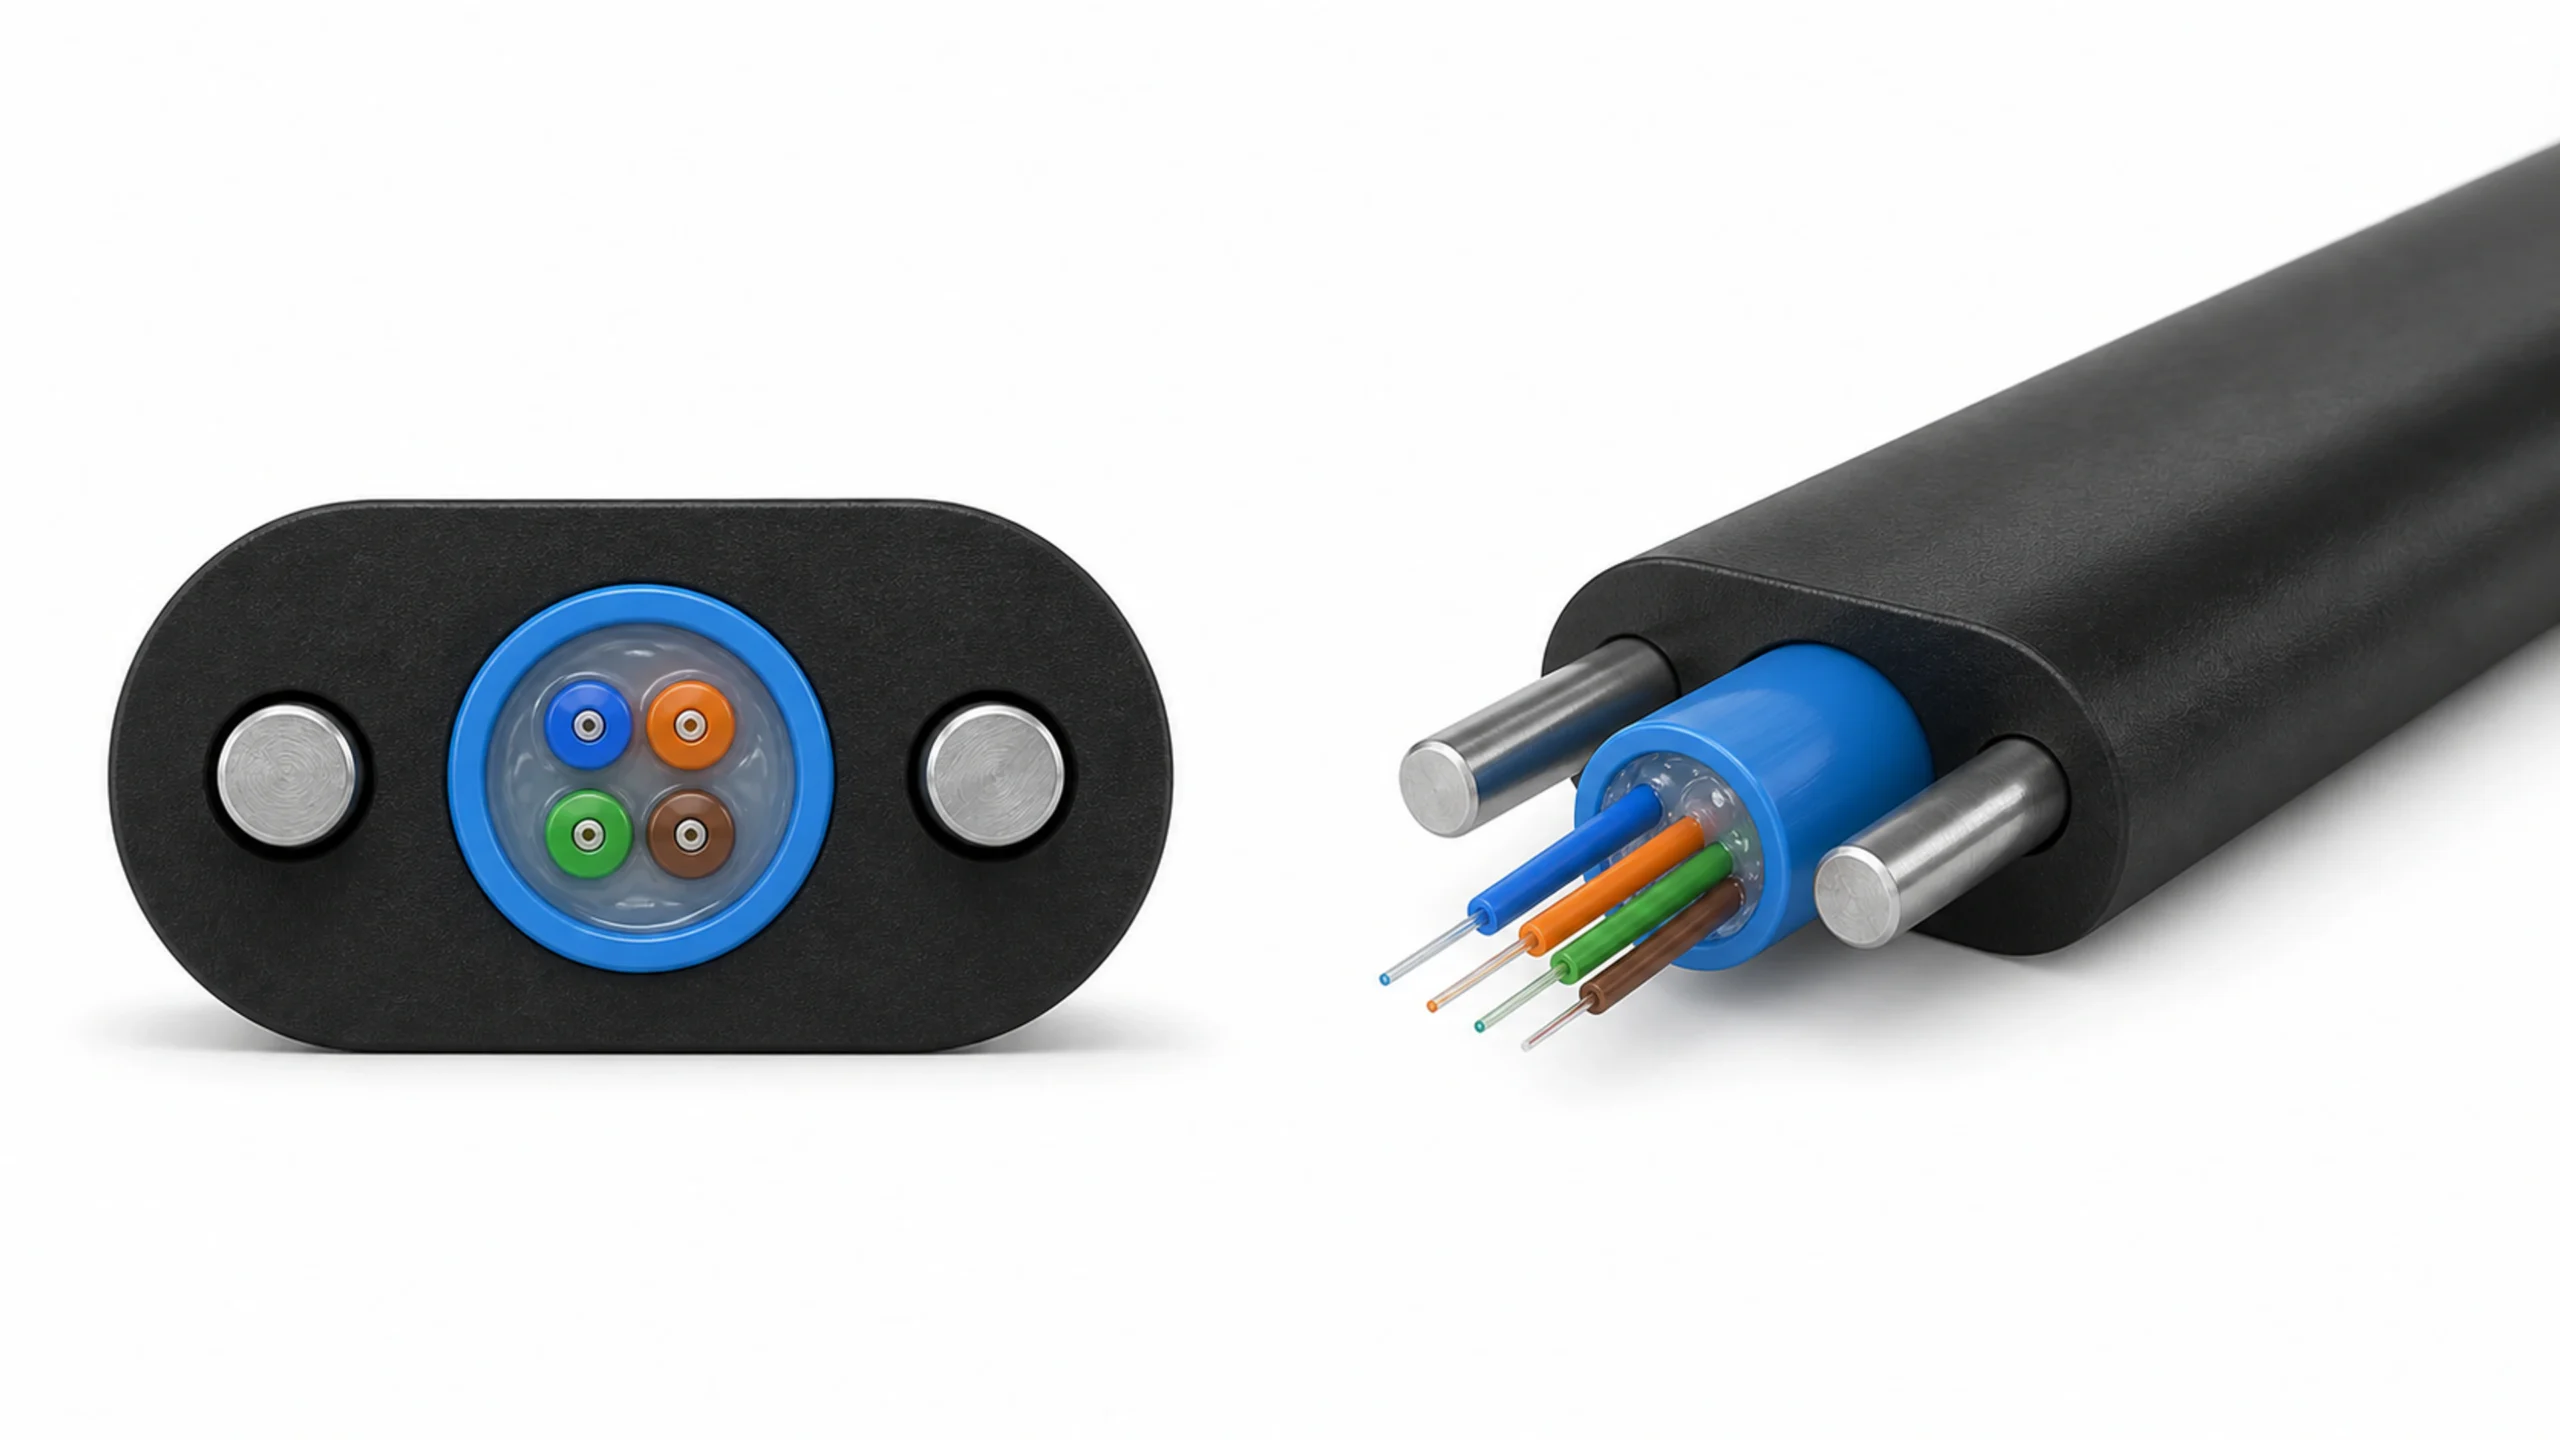
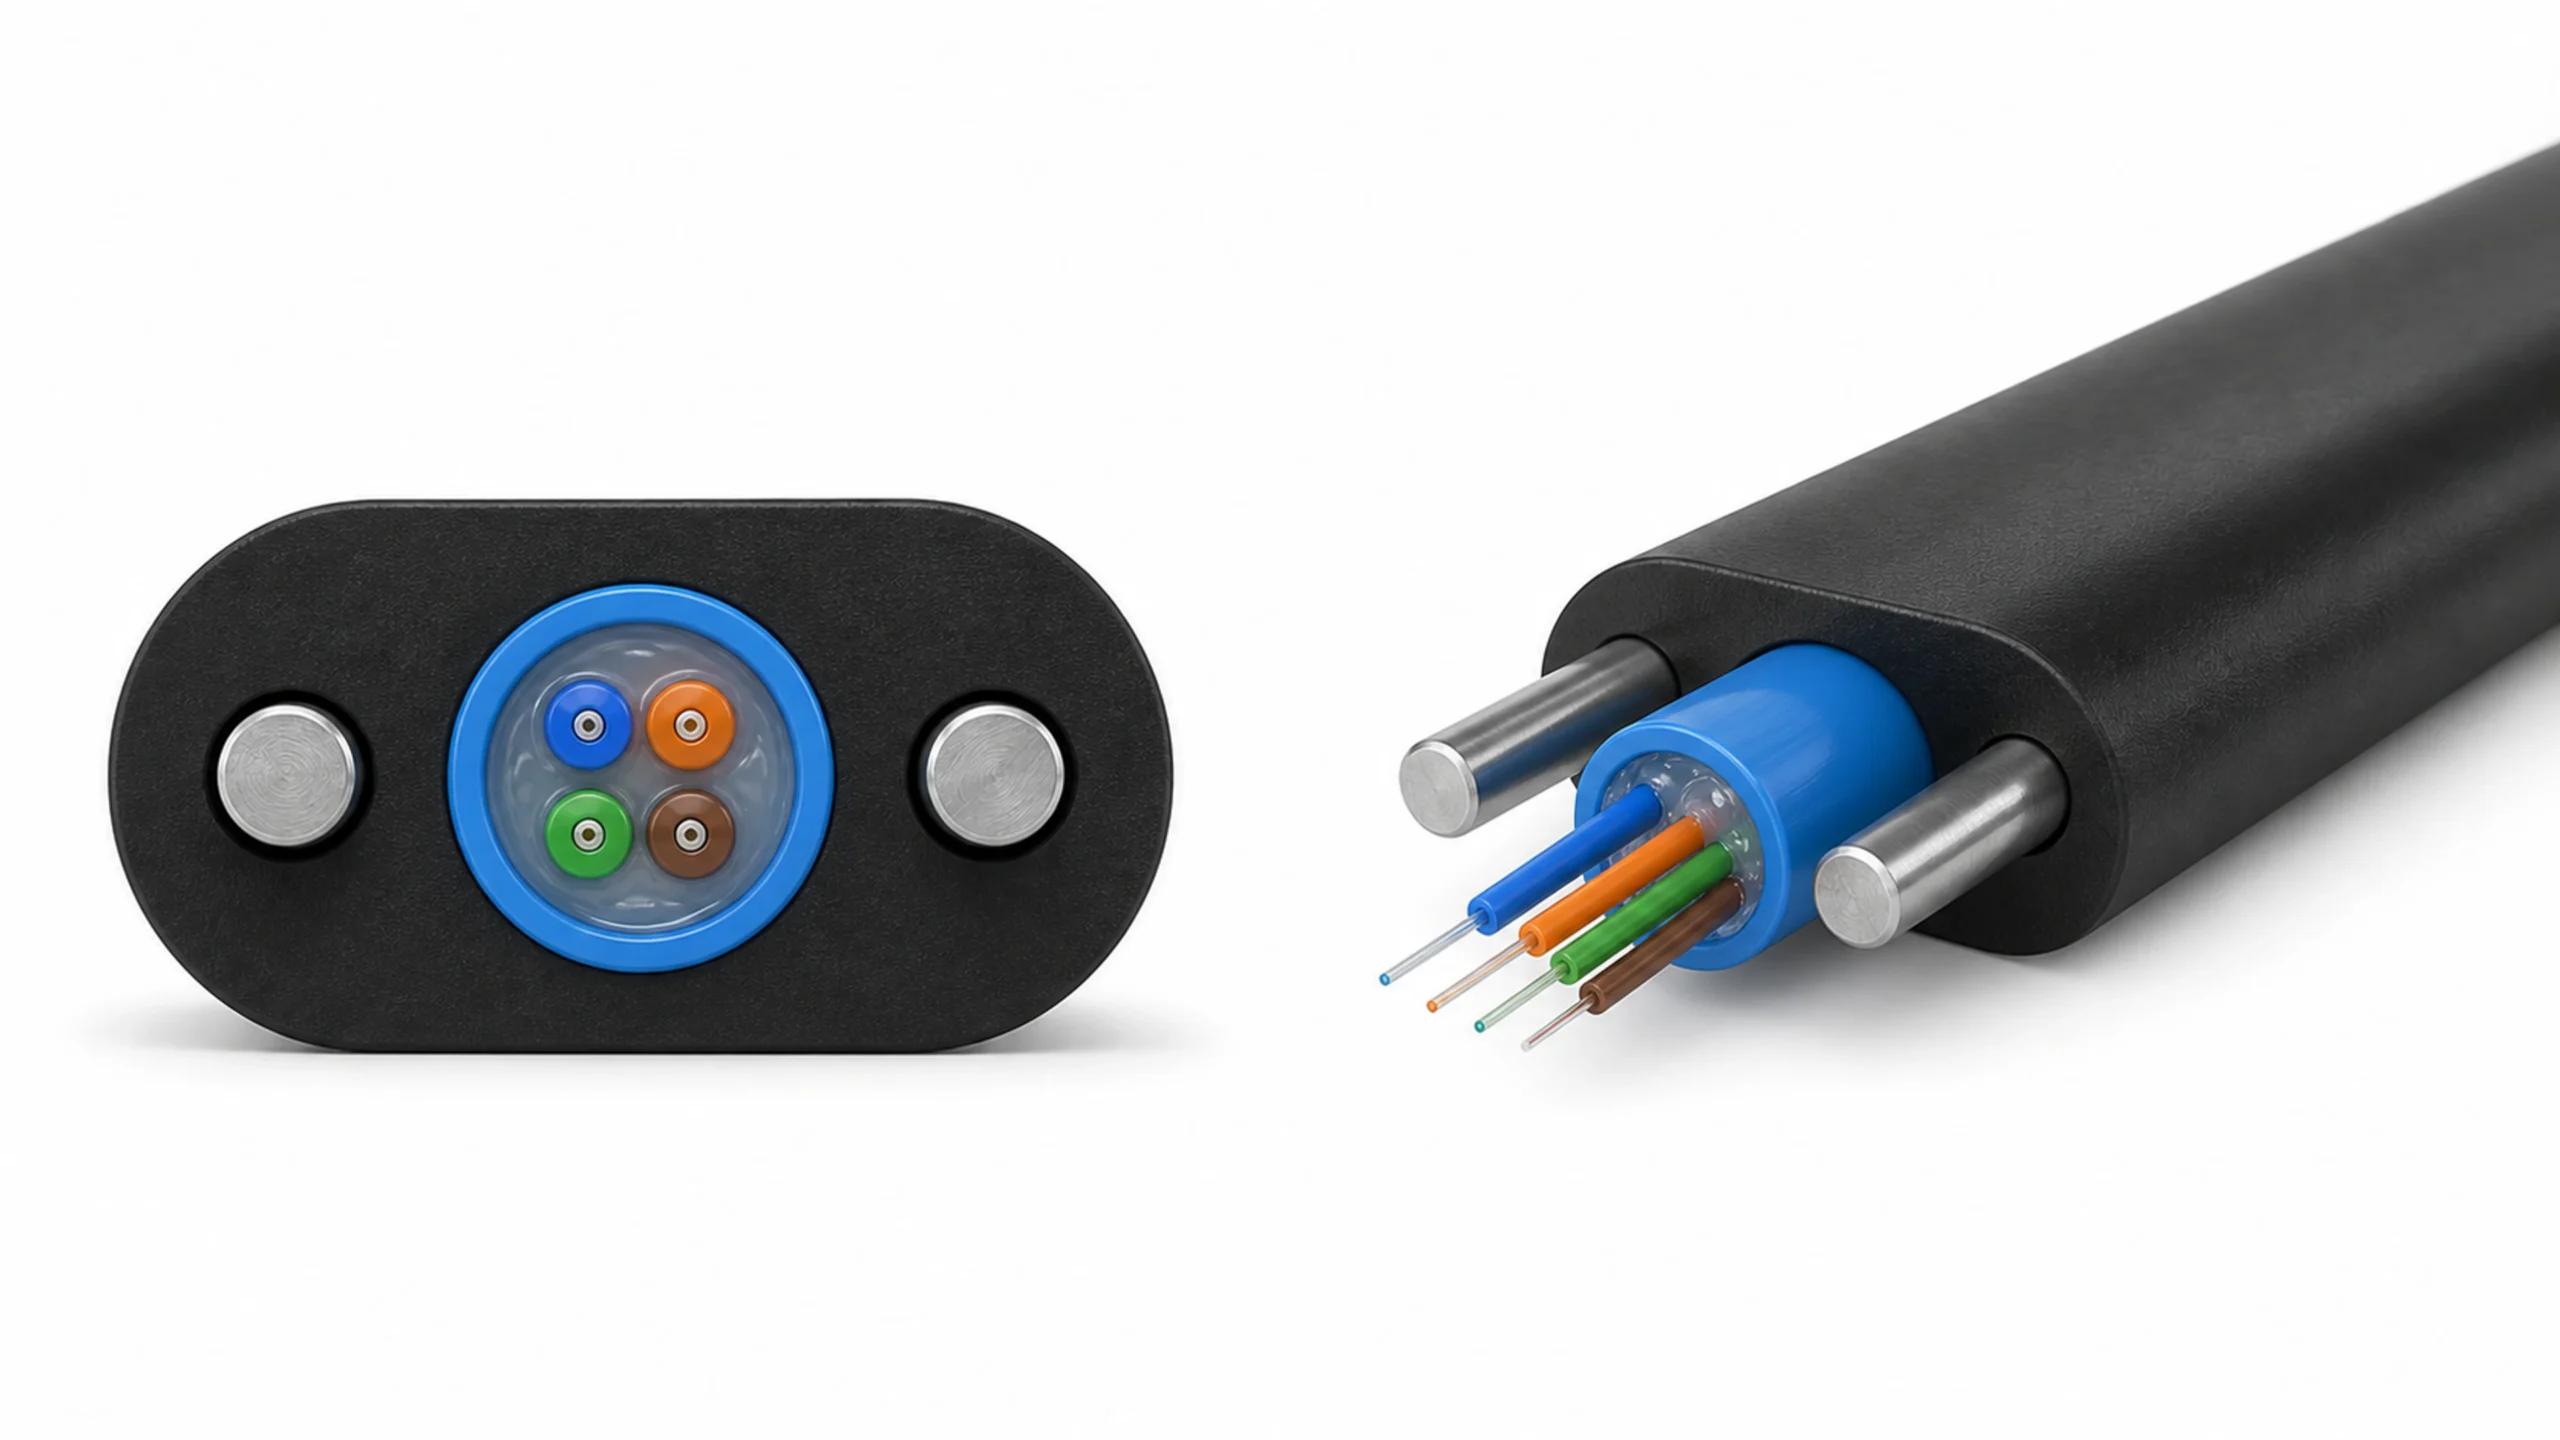
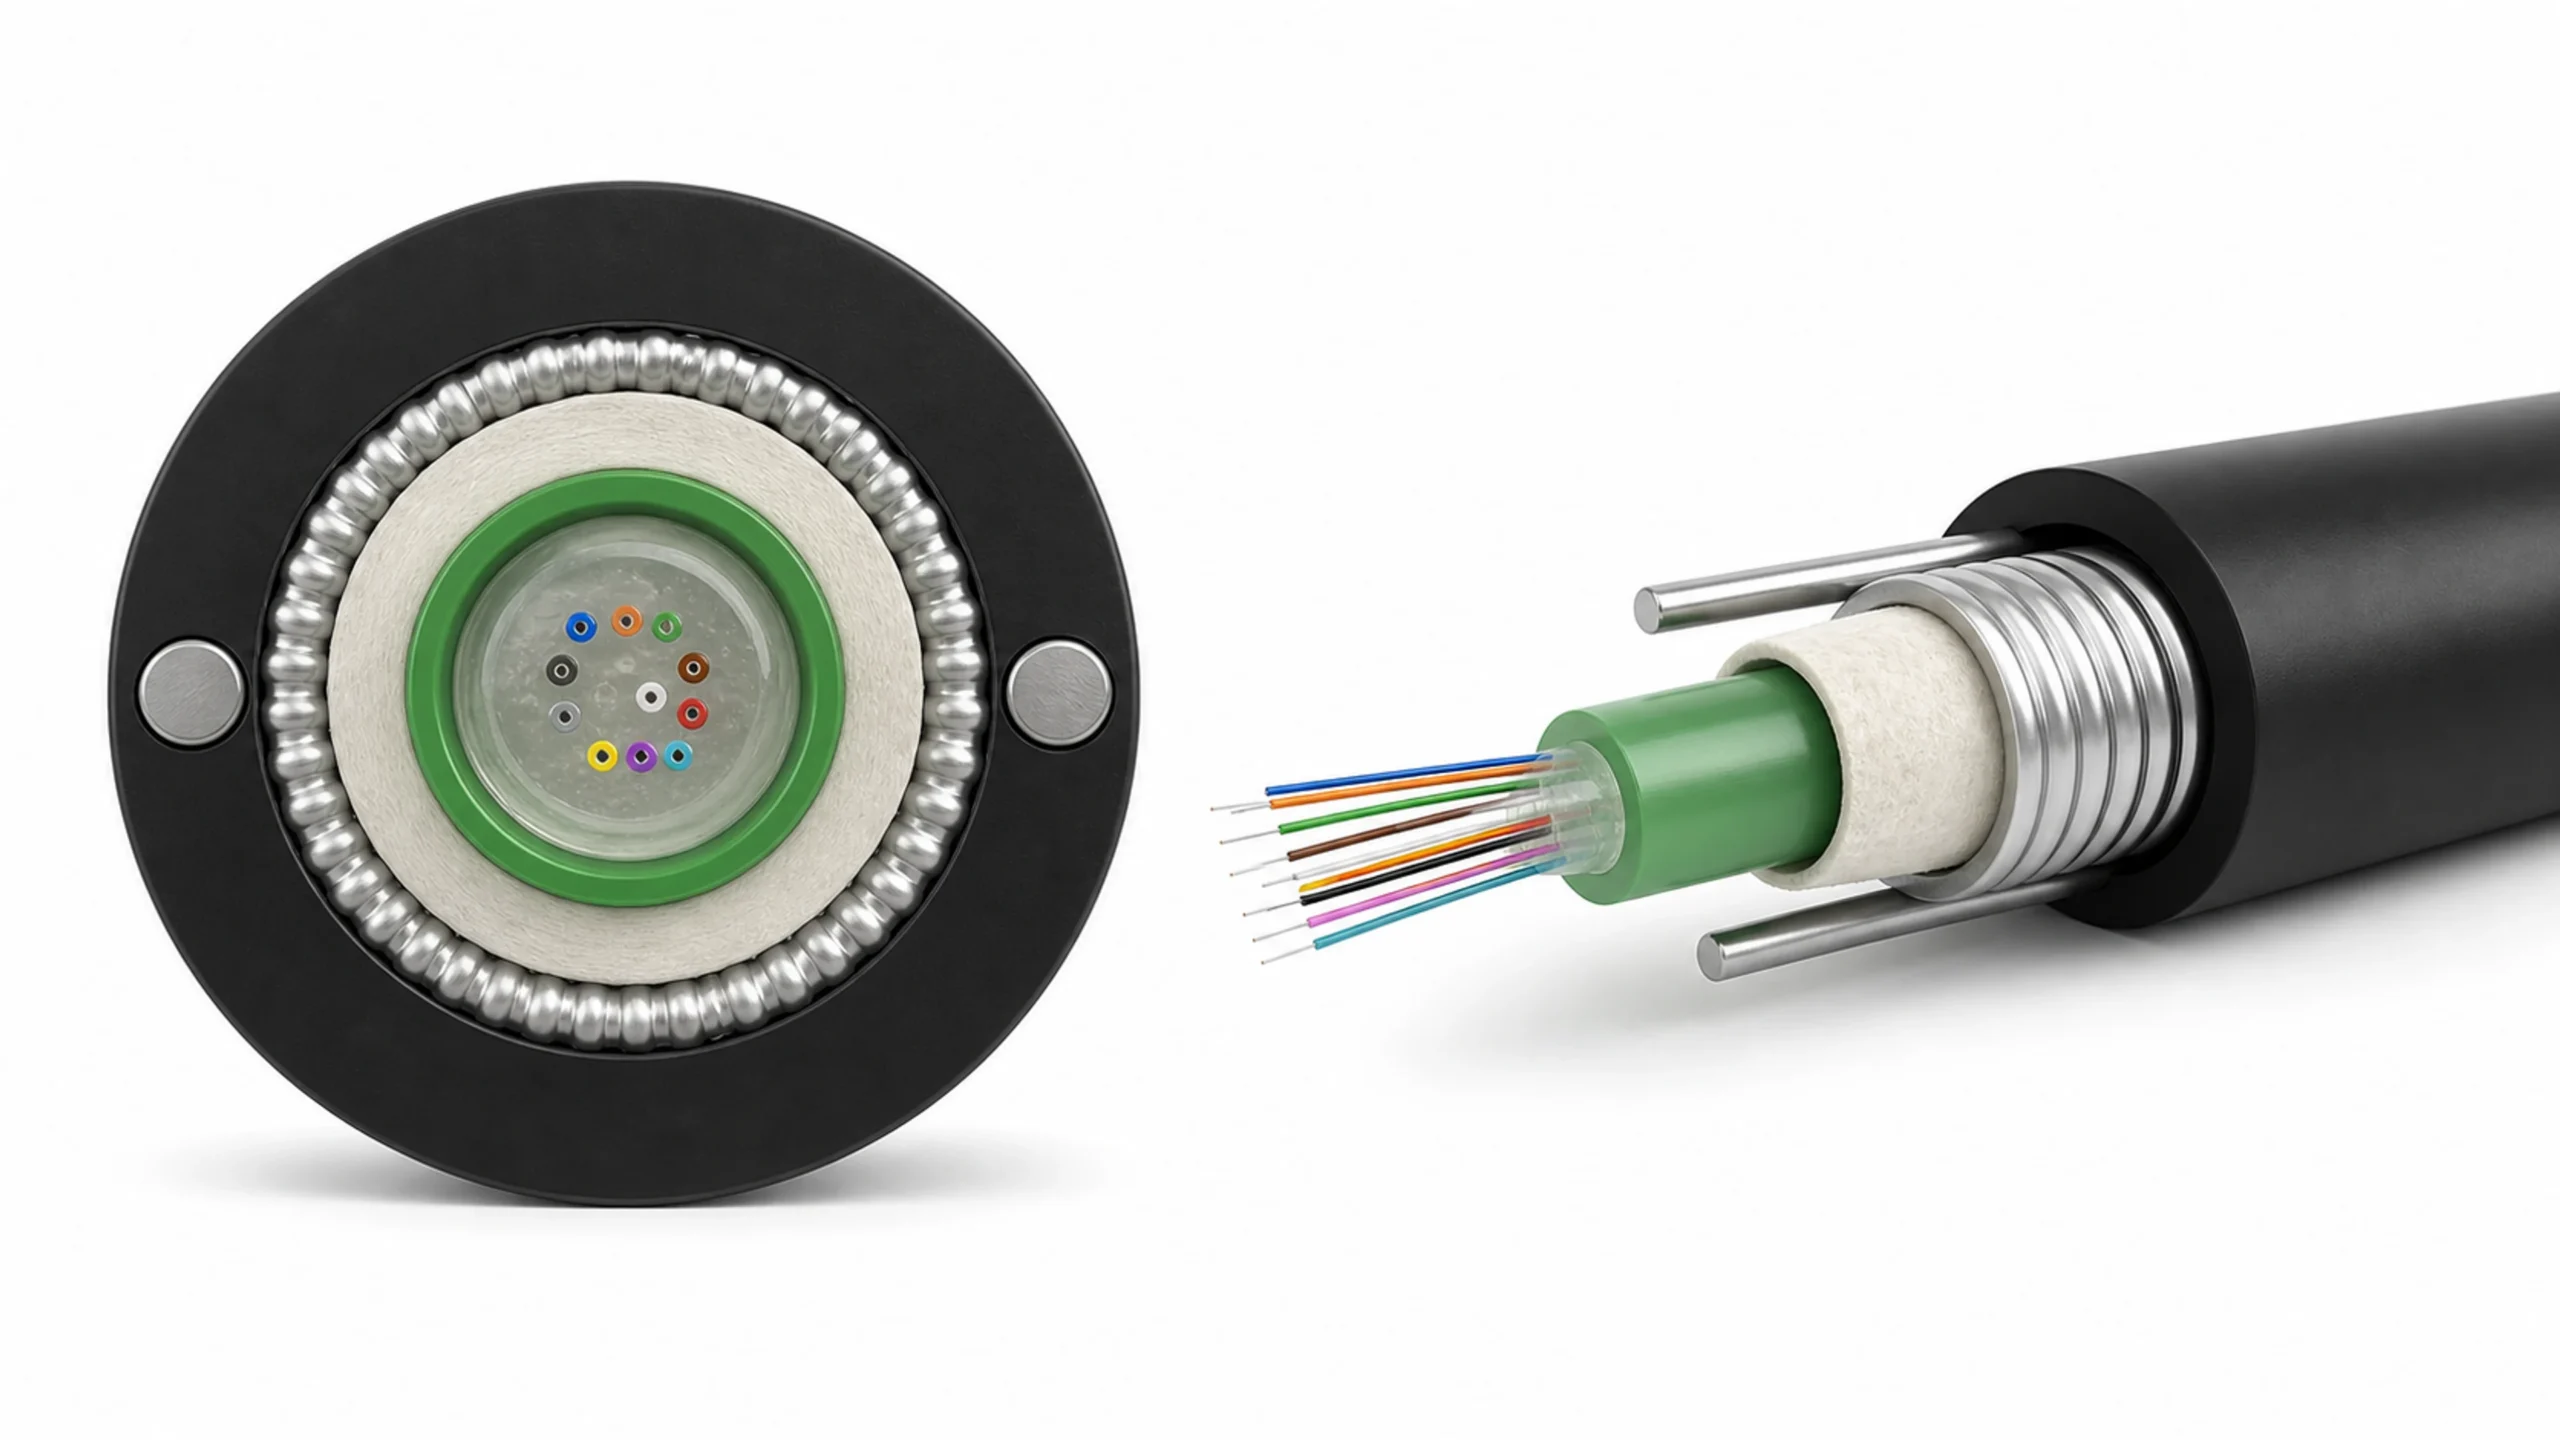
Construction matters: armored, all-dielectric and figure-8 cables require different preparation, reinforcement and tooling. One illustrated arrangement does not establish compatibility with every cable.
Veja o processo de revestimento. Planeje o ensaio de aceitação.
The HONGKAI HK-90 video shows a sheathing reference for an ADSS cable route. Use it to discuss equipment and operating sequence, then agree the trial for your construction.
01PRODUCT
Teste a construção especificada.
Utilize o núcleo aprovado, o composto de bainha, os materiais de proteção e o tambor de saída.
02PROCESS
Verifique o comportamento coordenado.
Observe a extrusão, resfriamento, monitoramento do diâmetro, tração e enrolamento durante as partidas, operação contínua e paradas.
03OUTPUT
Agree the inspection record.
Verifique o diâmetro final, a espessura da bainha e a aparência, a marcação, o enrolamento e os testes ópticos e de revestimento acordados.
ACCEPTANCE BASISDesenho aprovado + materiais acordados + condições operacionais + método de inspeção por escrito
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
01
Escopo do equipamento
Especifique os módulos fornecidos e as quantidades
Identify retained and buyer-supplied equipment
Registrar as responsabilidades da fonte do equipamento
02
Line integration
Revisar o layout e as interfaces de fluxo de material
Define controls, utilities and safety boundaries
Concordar com o escopo de instalação e comissionamento
03
Start-up & support
Definir produtos de teste e registros de aceitação
Confirm operator training and documentation
Agree spare-parts and after-sales scope
09START THE ENGINEERING REVIEW
Tell us about the cable you need to sheath.
Comece com seu desenho, requisitos do produto ou equipamento existente. Os detalhes técnicos podem ser confirmados durante a primeira revisão.
WHAT TO PREPARE
Nine inputs for your sheathing line.
01
Cable drawing and finished dimensions
02
Incoming core or loose-tube details
03
Sheath compound and jacket thickness
04
Reinforcement, tape and ripcord requirements
05
Input and output drum sizes / weights
06
Target output and operating plan
07
Marking, testing and acceptance criteria
08
Factory layout and retained equipment
09
Utilities, installation and project timing
10BUYER FAQ
Questions before specifying an HK-90 sheathing line.
Review the cable construction, equipment boundary and information needed for a proposal.
01O que a linha de revestimento HK-90 produz?
Aplica a bainha externa especificada a um núcleo de cabo óptico preparado ou a um tubo específico da construção e ao pacote de proteção, depois resfria, inspeciona e recolhe o cabo. A coloração da fibra a montante, a extrusão do tubo solto e o encordoamento SZ são etapas separadas, salvo se incluídas no escopo do projeto.
02É possível uma única linha produzir cabos GYXTW, ADSS e em forma de 8?
Essas famílias de cabos podem envolver uma etapa de revestimento HK-90, mas não utilizam um pacote de equipamentos idêntico. O manuseio do núcleo, reforço, armadura, posicionamento do mensageiro, ferramental da cabeçote cruzada e testes a jusante devem ser analisados para cada desenho de cabo.
03Toda configuração inclui equipamento de fita metálica?
Nº. Selecionam-se desenrolamento de fita metálica, junção, acumulação, corrugação e formação longitudinal para a construção especificada com armadura ou bainha composta. Uma rota totalmente dielétrica tem requisitos diferentes de reforço.
04O que significam a velocidade e a saída cotadas?
The reference ratings are up to 80 m/min for PE cable below 10 mm and an extrusion-output reference of up to 250 kg/h PE with the crosshead open. These values describe stated reference conditions. Actual accepted cable output must be agreed for the cable, compound, tooling, cooling and operating plan.
05Quais compostos de bainha podem ser utilizados?
A referência da extrusora fornecida descreve PE e PVC. Confirme a classe exata e as configurações necessárias de parafuso, ferramental, secagem e temperatura. Não presuma que LSZH ou outro composto esteja coberto sem uma análise técnica separada.
06É incluído um acumulador de cabo acabado?
A referência do equipamento inclui um acumulador de fita metálica, que armazena a fita para sua sequência de junção. Um acumulador de cabo acabado desempenha uma função diferente e requer sua própria configuração, tensão, comprimento de armazenamento e revisão de troca de bobina.
07O verificador de faíscas do revestimento pode ser usado para ADSS?
A aplicabilidade do teste depende da construção do cabo e de um caminho de retorno elétrico adequado. Um cabo totalmente dielétrico não deve ser automaticamente submetido ao mesmo arranjo de teste de centelhamento que um cabo contendo metal. Confirme o método de teste e os critérios de aceitação para o produto real.
08O que devo enviar para um orçamento?
Envie o desenho do cabo, o núcleo de entrada, o composto da bainha, os materiais de proteção, os tamanhos necessários dos tambores e a meta de produção. Adicione o layout da sua fábrica e as máquinas existentes, se disponíveis. Os detalhes técnicos podem ser preenchidos durante a primeira revisão.
We've detected you might be speaking a different language. Do you want to change to:





 English
 हिन्दी
 فارسی