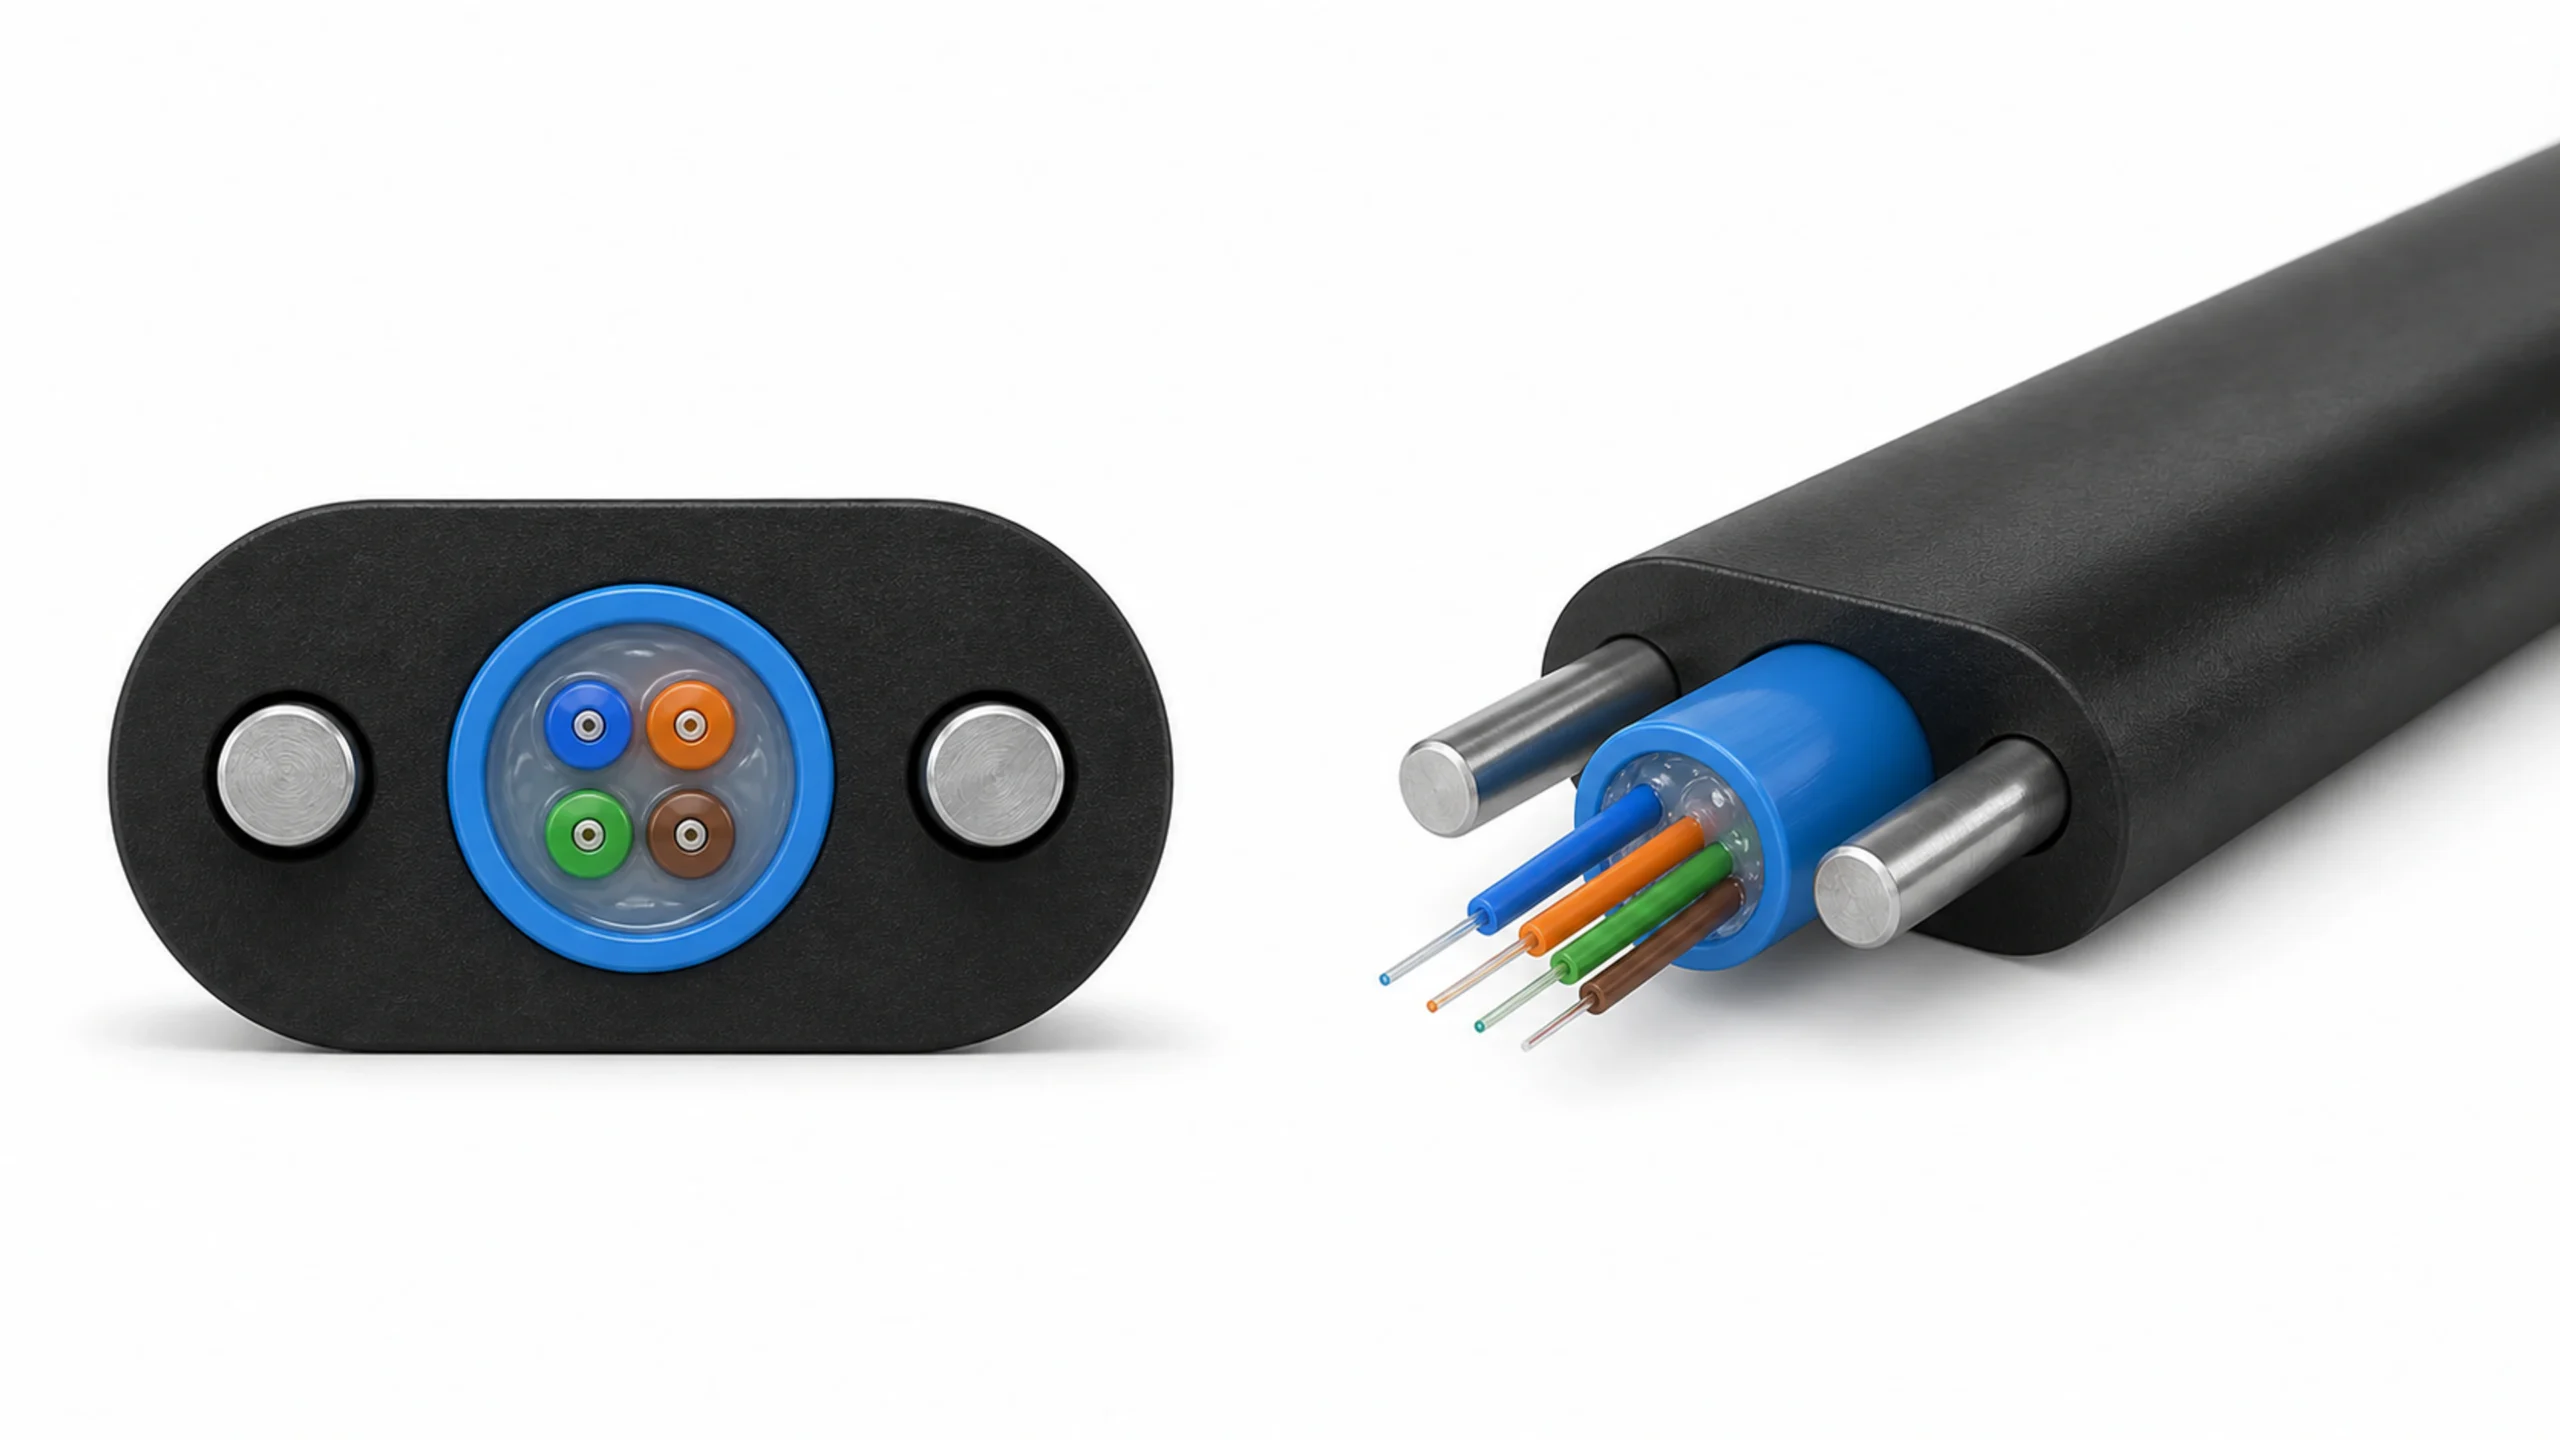
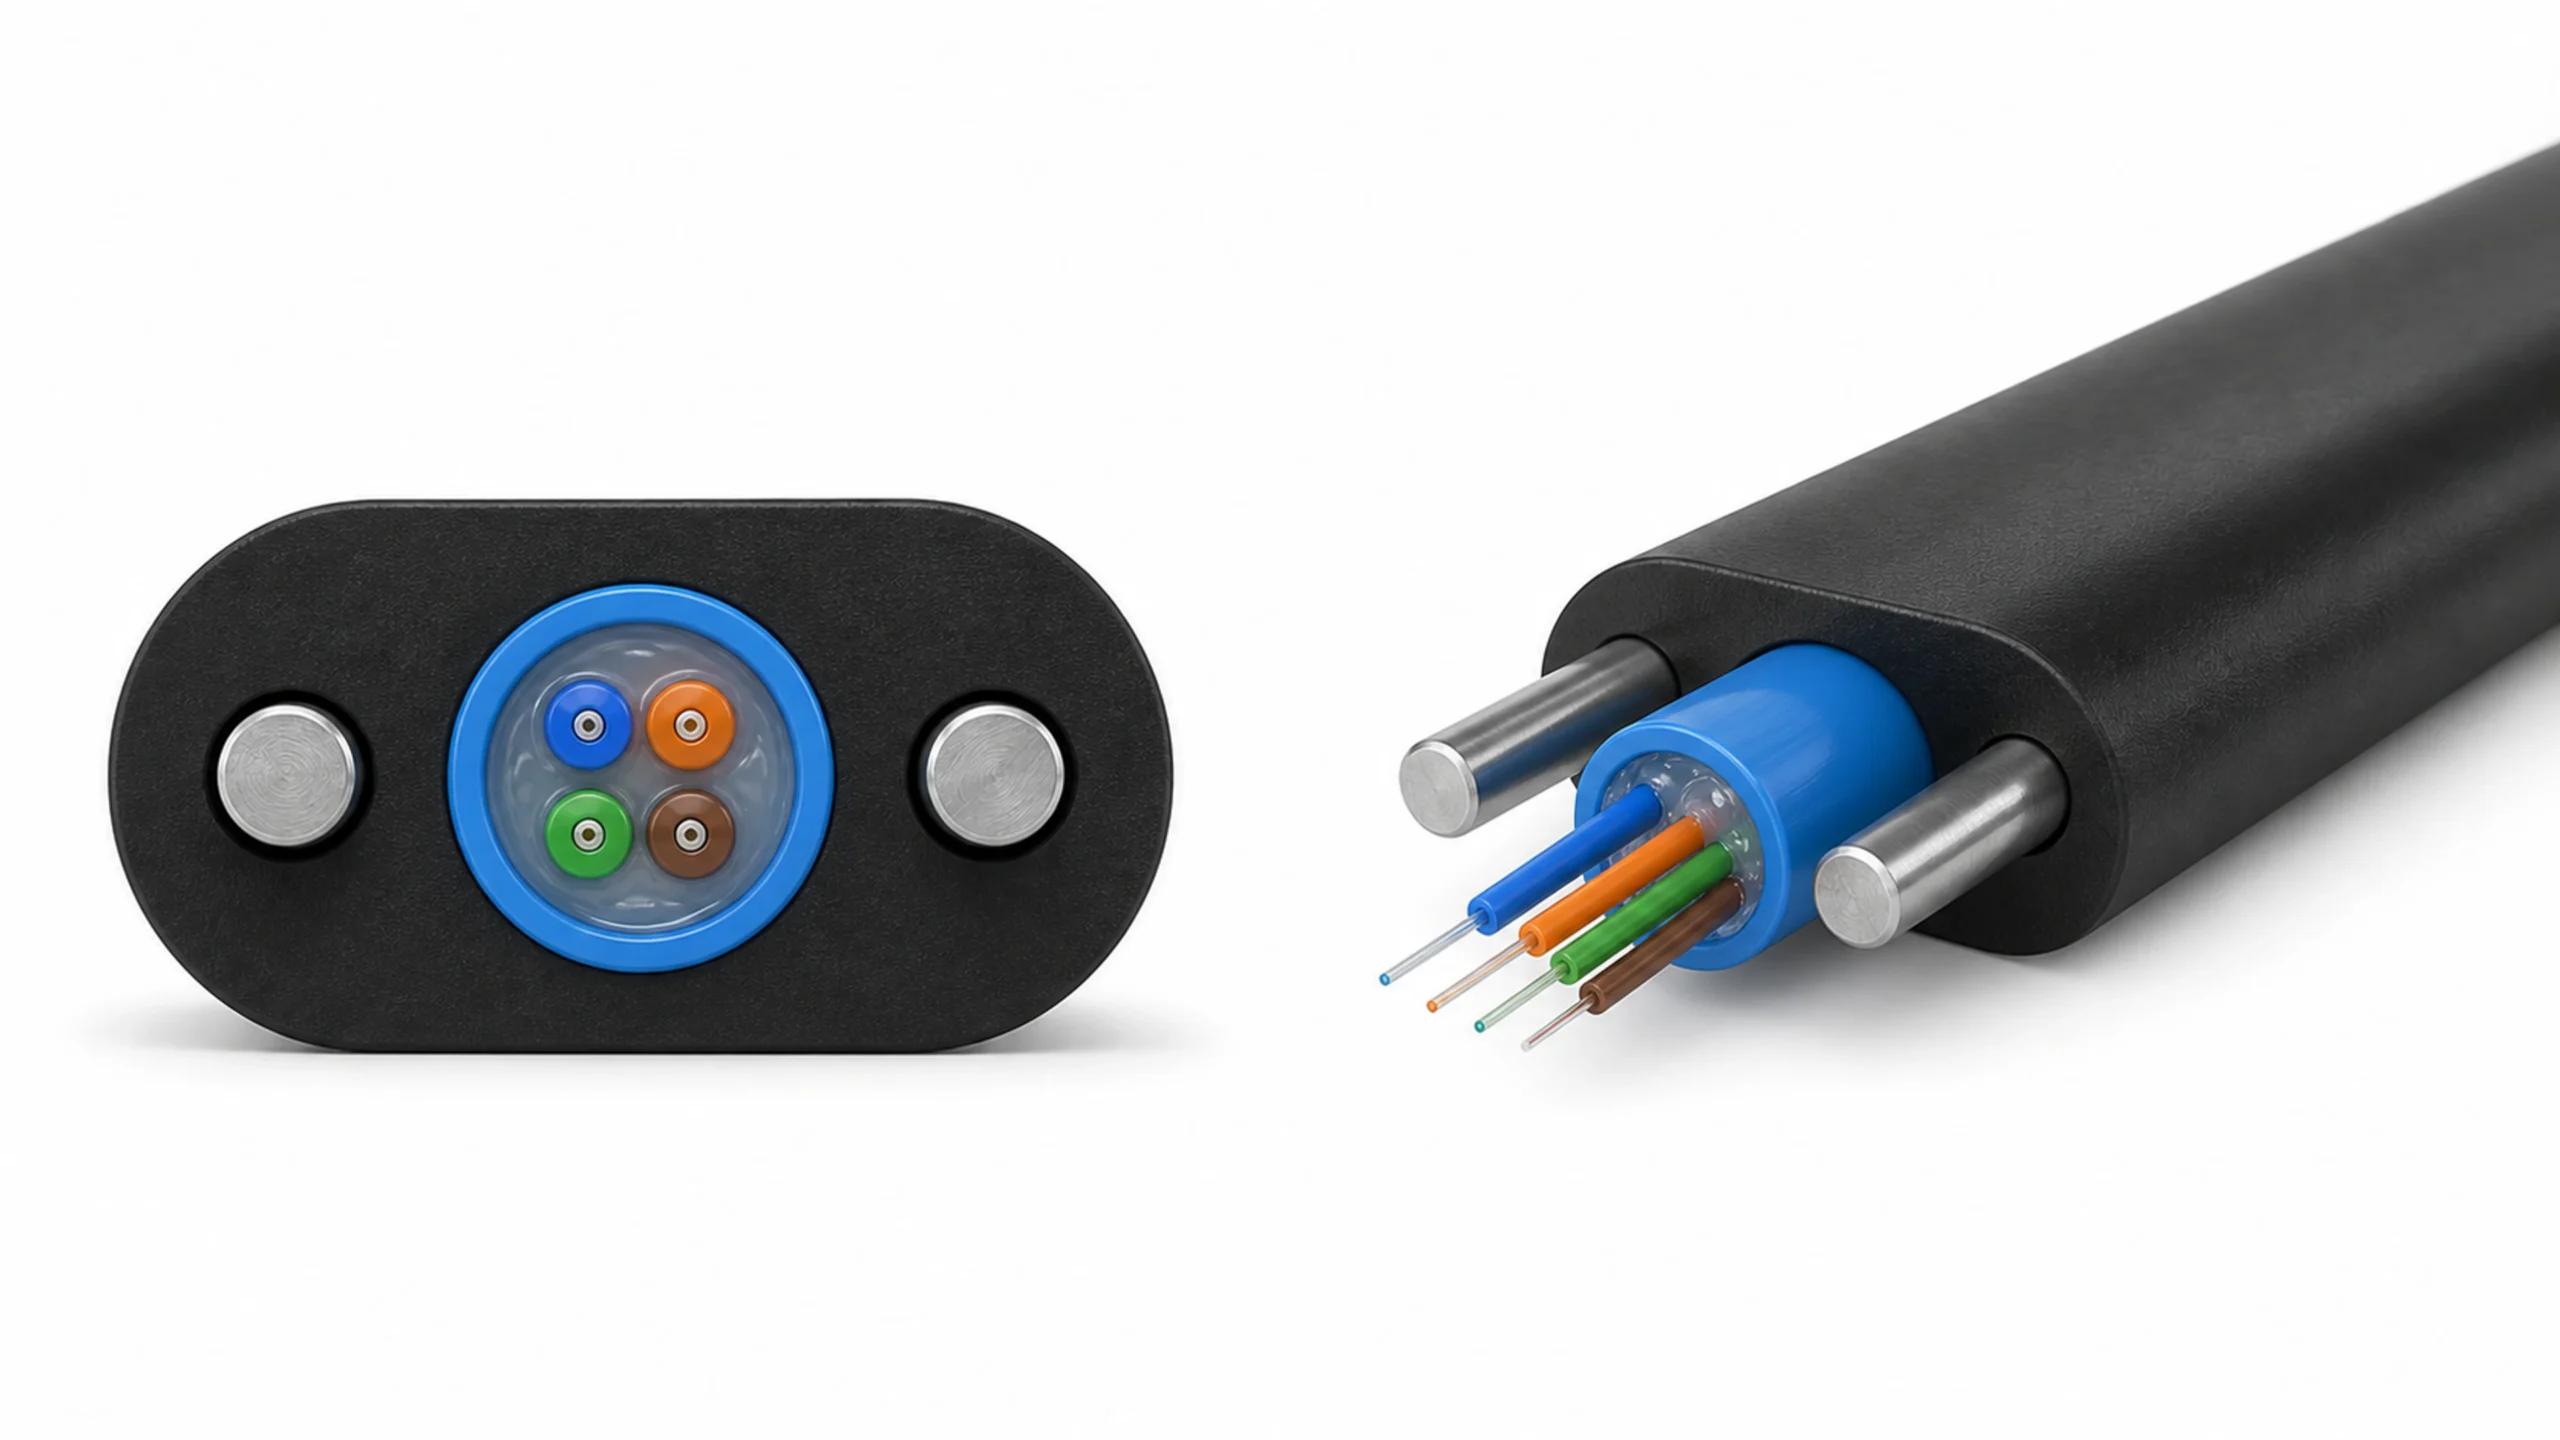
Coordinate melt delivery, tooling, cooling and traction around the cable design.
المنتجات والإنتاج
ابدأ بالكابل الذي تريد تصنيعه.
قطع غيار لآلات HONGKAI.
استكشف الأجزاء حسب خط الإنتاج
تحقق من الصور واللوحات التعريفية وأرقام القطع
أرسل تفاصيل الماكينة والصور والكمية
تخطط لمصنع كامل؟
وصِّل منتجك وخطوط الإنتاج واحتياجات المواد الخاصة بك.
COMPLETE FACTORY SOLUTIONS
اتخذ قرارات مستنيرة قبل أن تستثمر.
فهم مدخلات الاستثمار
راجع دراسة العملية
قارن بين اللفة الثلاثية واللفة المزدوجة
منتجك هو نقطة البداية.
خطّط المعدات والمواد والمصنع حولها.
Φ90 mm extrusion · Core pay-off to finished cable take-up
USD 118,900 per set
Quoted configuration: HK-90 PLC+IPC Control Outdoor Optical Cable Sheathing Production Line. Ex-factory delivery; the buyer arranges and pays transport. Final equipment and tooling follow the agreed configuration schedule.
Apply the specified outer sheath around your prepared optical cable core. Configure material feeding, aramid yarn stranding or metal-tape protection as required, extrusion, cooling and take-up as one coordinated production stage.

Coordinate melt delivery, tooling, cooling and traction around the cable design.
Scope boundary: this page covers the sheathing stage. Upstream coloring, loose-tube extrusion and SZ core stranding are separate processes. Reinforcement and armoring modules are selected for the approved cable construction.
Build the process around the cable layers. Optional protection modules are selected before the extrusion and downstream handling requirements are finalized.
Start with the prepared core or loose tube. Match the core, wire and protection-material pay-offs to the incoming package.
Apply the selected water blocking and ripcord. ADSS routes add aramid yarn stranding before the outer sheath; armored routes use the specified metal-tape preparation and forming modules.
Feed the approved compound to the Φ90 mm extruder and crosshead. Coordinate melt delivery, cable centering, temperature and line speed.
Cool and dry the sheath, monitor diameter, apply the specified marking and tests, then coordinate caterpillar traction with finished-cable take-up.
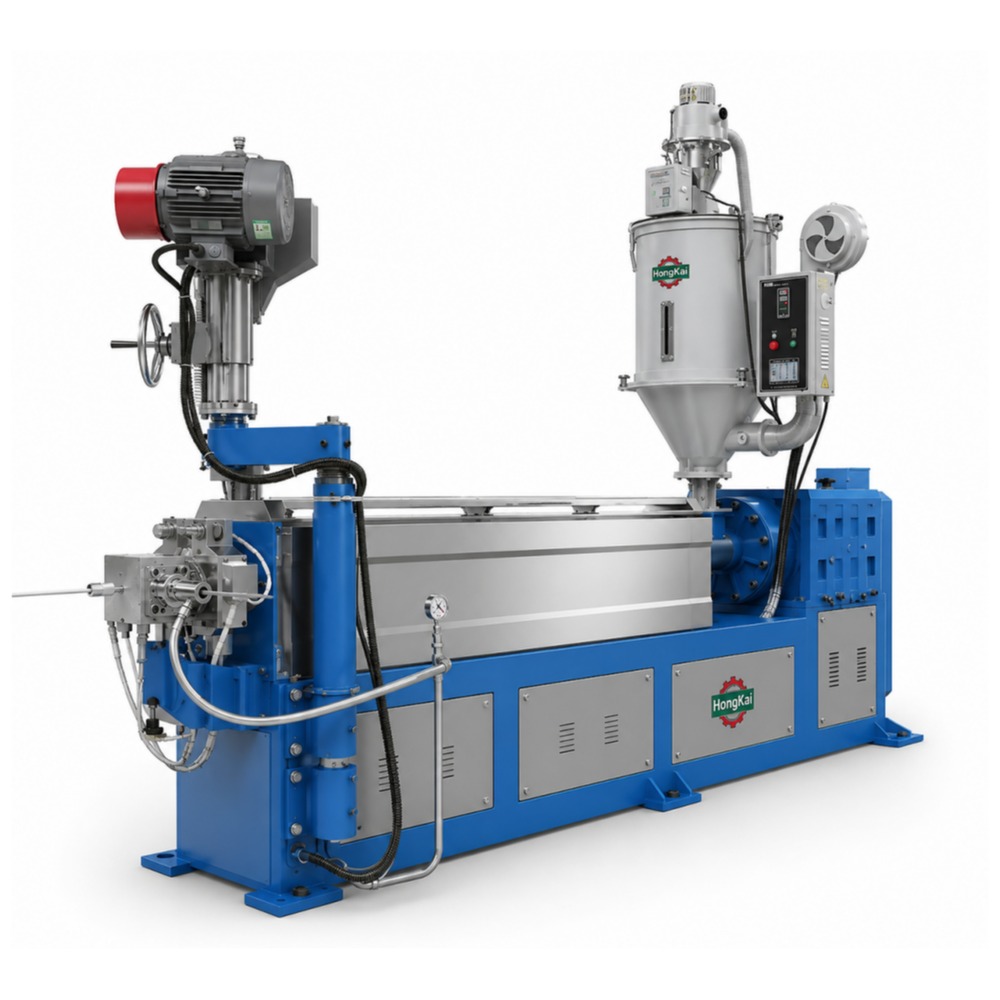
Rotate the HK-90 line, select a device for a closer look, and compare its exterior with the original equipment photograph.
Preparing the interactive line…
The interactive view could not finish loading. Retry the 3D view, or use the equipment references on this page.
Illustrative exterior study. Final equipment, dimensions and layout follow the approved project configuration.
The same extrusion stage can sit within different process routes. Compare the incoming core, reinforcement and tape requirements before defining the equipment package.
Select a number or equipment card to see its equipment area, image and process role. Dashed regions identify process interfaces whose final position must be confirmed. The reference includes optional preparation and testing modules; the final equipment list follows your cable construction.
13 · Φ90 mm sheath extruderEquipment area in the reference arrangement

Equipment shown is for reference. Final construction and quantity follow your approved equipment list.
Plasticizes the approved sheath compound and supplies the adjustable crosshead. The reference uses a Φ90 mm screw with a 25:1 L/D ratio.
درجة المركب، البرغي والرأس المتصالب، الأدوات، منحنى درجة الحرارة، الناتج وأبعاد الغلاف المطلوبة.
Selected equipment 13: Φ90 mm sheath extruder
Reference boundary: the panorama illustrates equipment order, not the final machine count, footprint or construction. The approved layout and equipment list define machine quantities, dimensions and the supplied arrangement.
Use the reference below to begin the technical review. Confirm the complete cable construction, material grade and trial conditions before agreeing production performance.
| Review area | Reference / requirement | Condition to confirm |
|---|---|---|
| Extruder reference | Φ90 mm screw · 25:1 L/D · 75 kW main drive. | Reference equipment configuration; screw, crosshead and tooling must suit the compound and cable. |
| Aramid stranding reference | 24 heads · independent tension · adjustable pitch · S or Z lay. | Selected for the cable construction. Confirm yarn grade, quantity, tension and stranding pitch together with extrusion speed. The reference 120 rpm rotation is not a cable line speed. |
| Sheath materials | PE / PVC for the reference extruder configuration. | Confirm the compound grade and process settings. Other compounds require a separate suitability review. |
| سرعة الإنتاج | Reference: up to 80 m/min for PE cable below Φ10 mm. | Reference value; confirm the complete construction, jacket thickness, cooling, reel changes and quality targets. |
| Extrusion output | Reference: up to 250 kg/h PE, with the crosshead open. | An extruder-output reference is not guaranteed finished-cable throughput. Verify it with the agreed tooling and compound. |
| Cable & tooling range | Specify incoming core, finished diameter and jacket thickness. | Review every module. A metal-tape forming tool may have a narrower range than the extruder or capstan. |
| Reels, tension & utilities | Agree supply/output drums, winding tension, layout and utility loads. | Use one approved schedule for the chosen configuration; do not infer these values from the HK-90 name. |
| Controls & acceptance | PLC / IPC coordination, recipes, alarms and agreed inspection records. | Define instruments, interfaces, safety functions, trial duration and acceptance criteria. |
Review output together with the sheath cross-section, compound, tooling and cooling capacity. Reel capacity, line footprint, tension settings and utility loads are finalized for the selected configuration.
Compare the complete cable route, then define the sheathing equipment and construction-specific preparation modules.

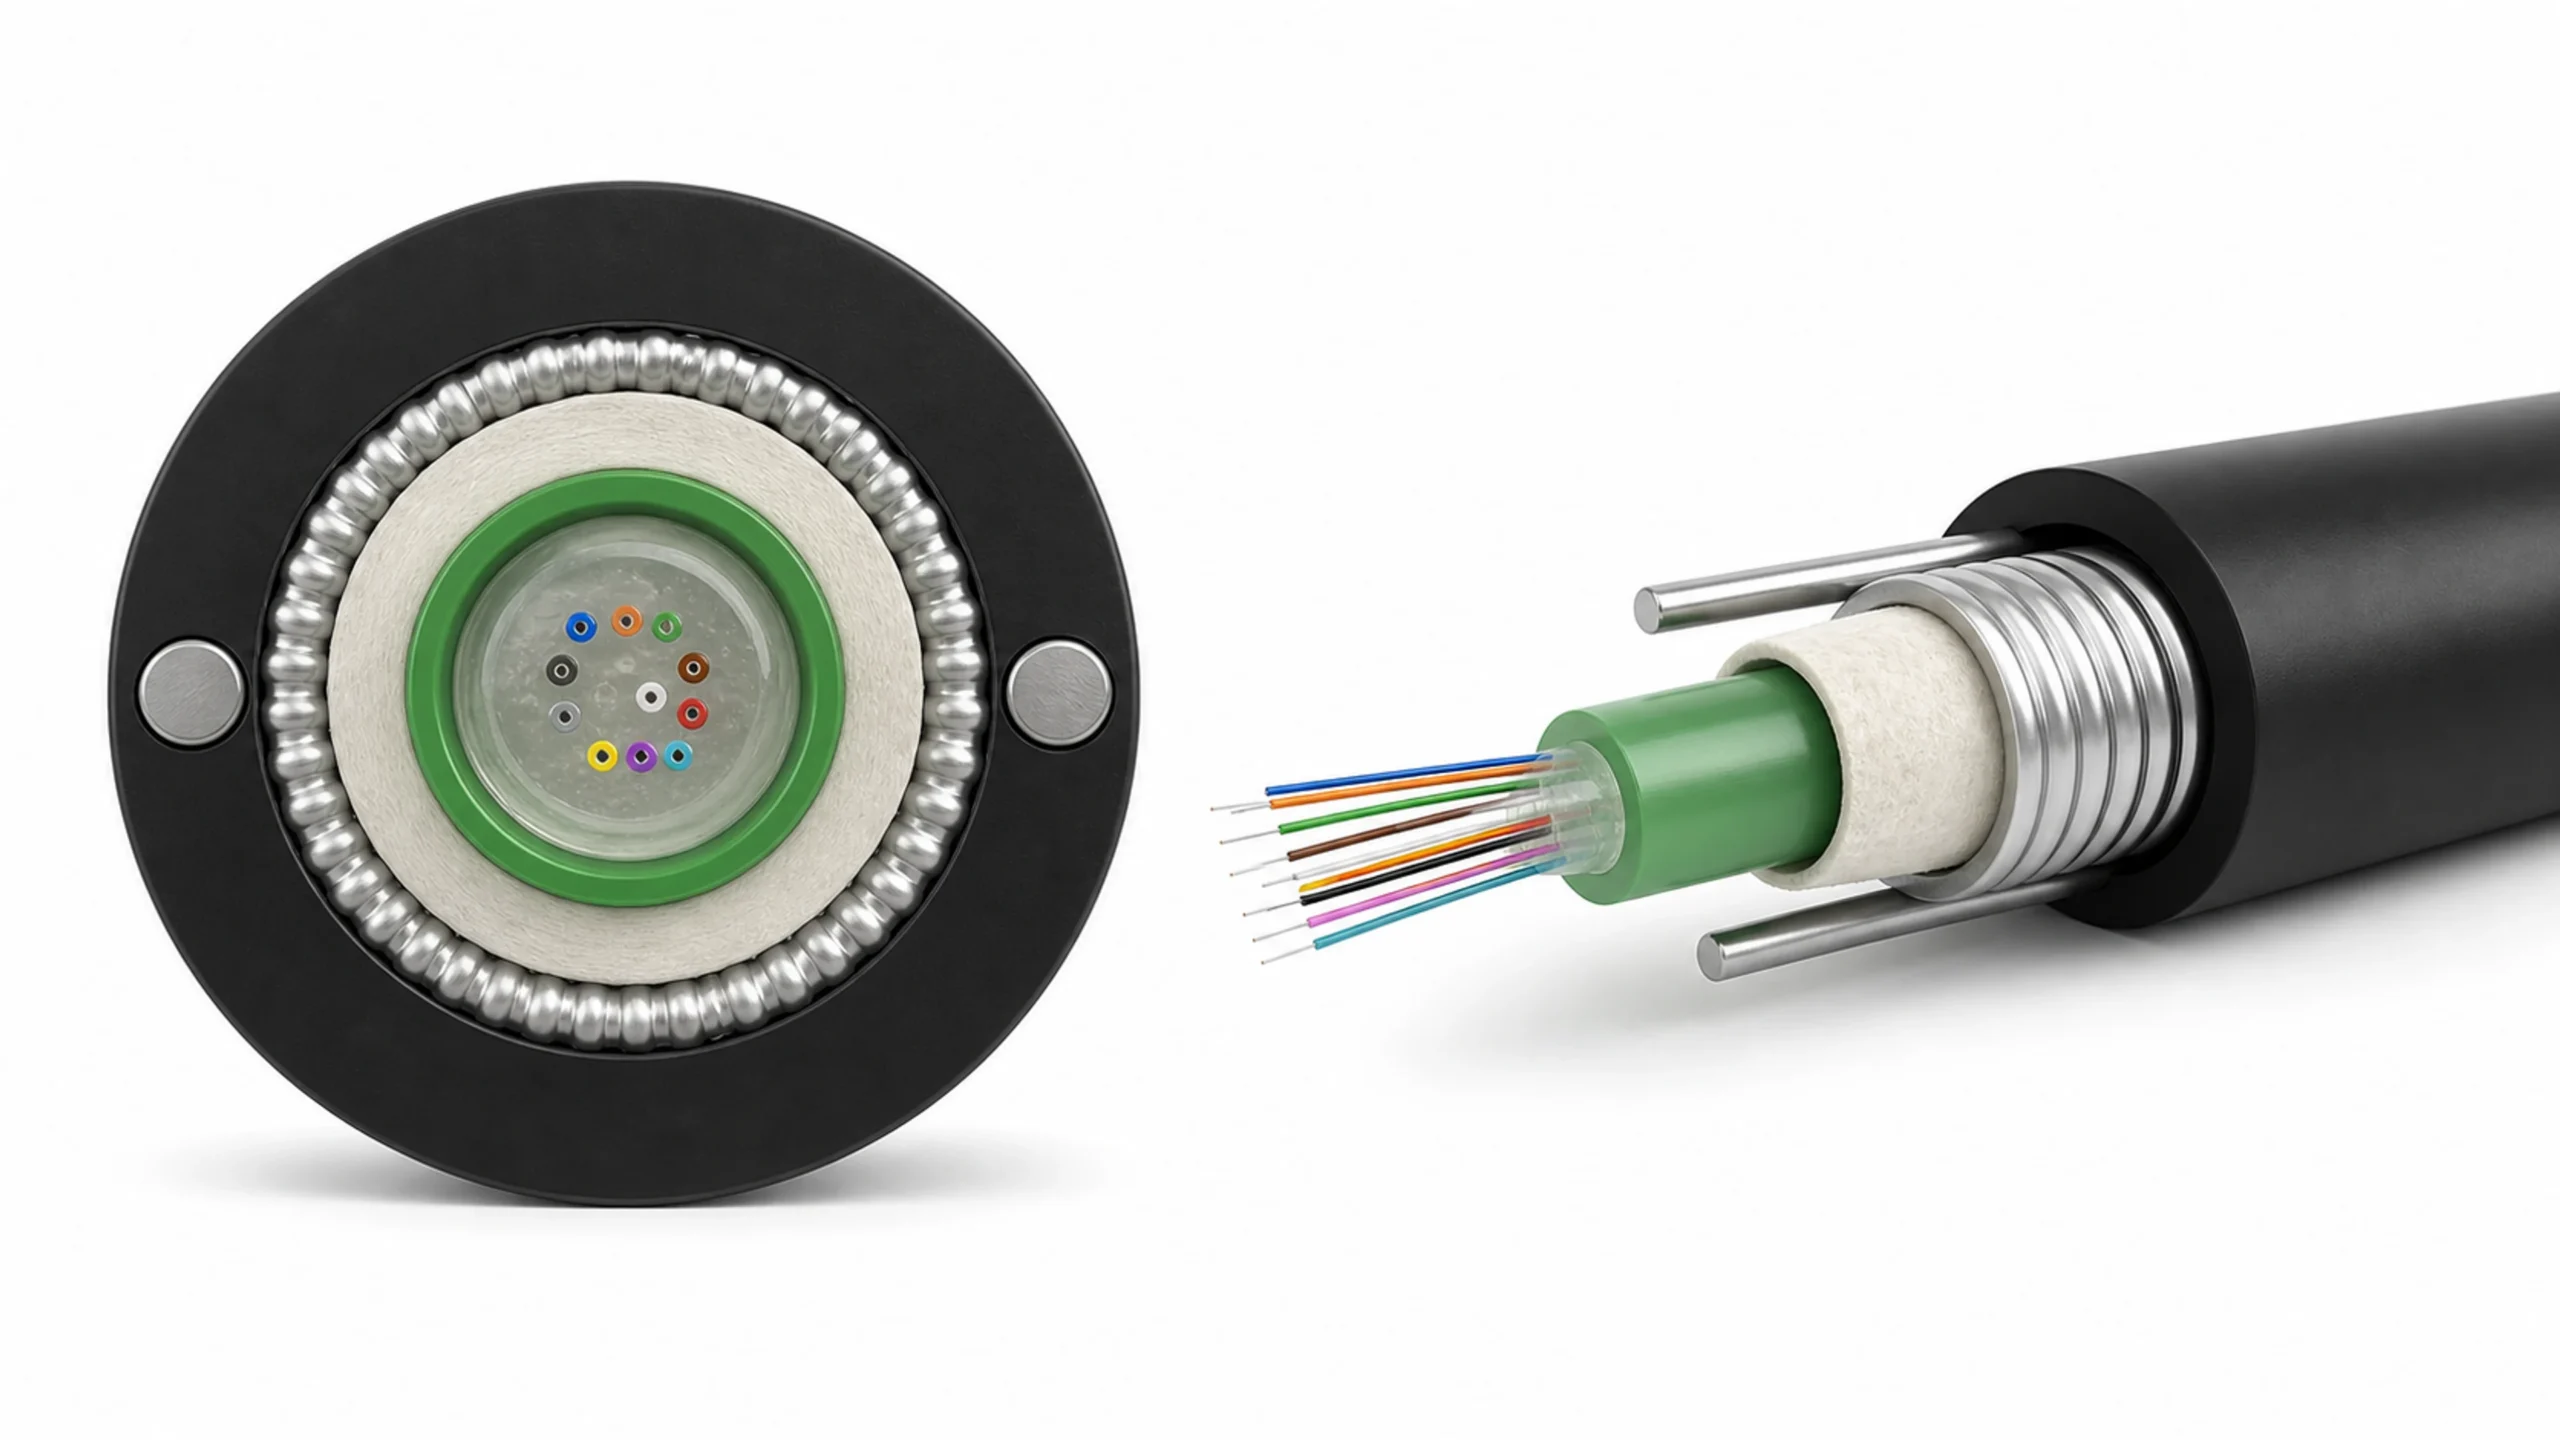
Review the loose-tube input, parallel strength members, metal-tape protection and outer-sheath requirements.
Open cable solution
Coordinate aramid yarn stranding with outer-sheath extrusion; confirm whether the incoming cable is a prepared core or an inner-sheathed cable.
Open cable solution
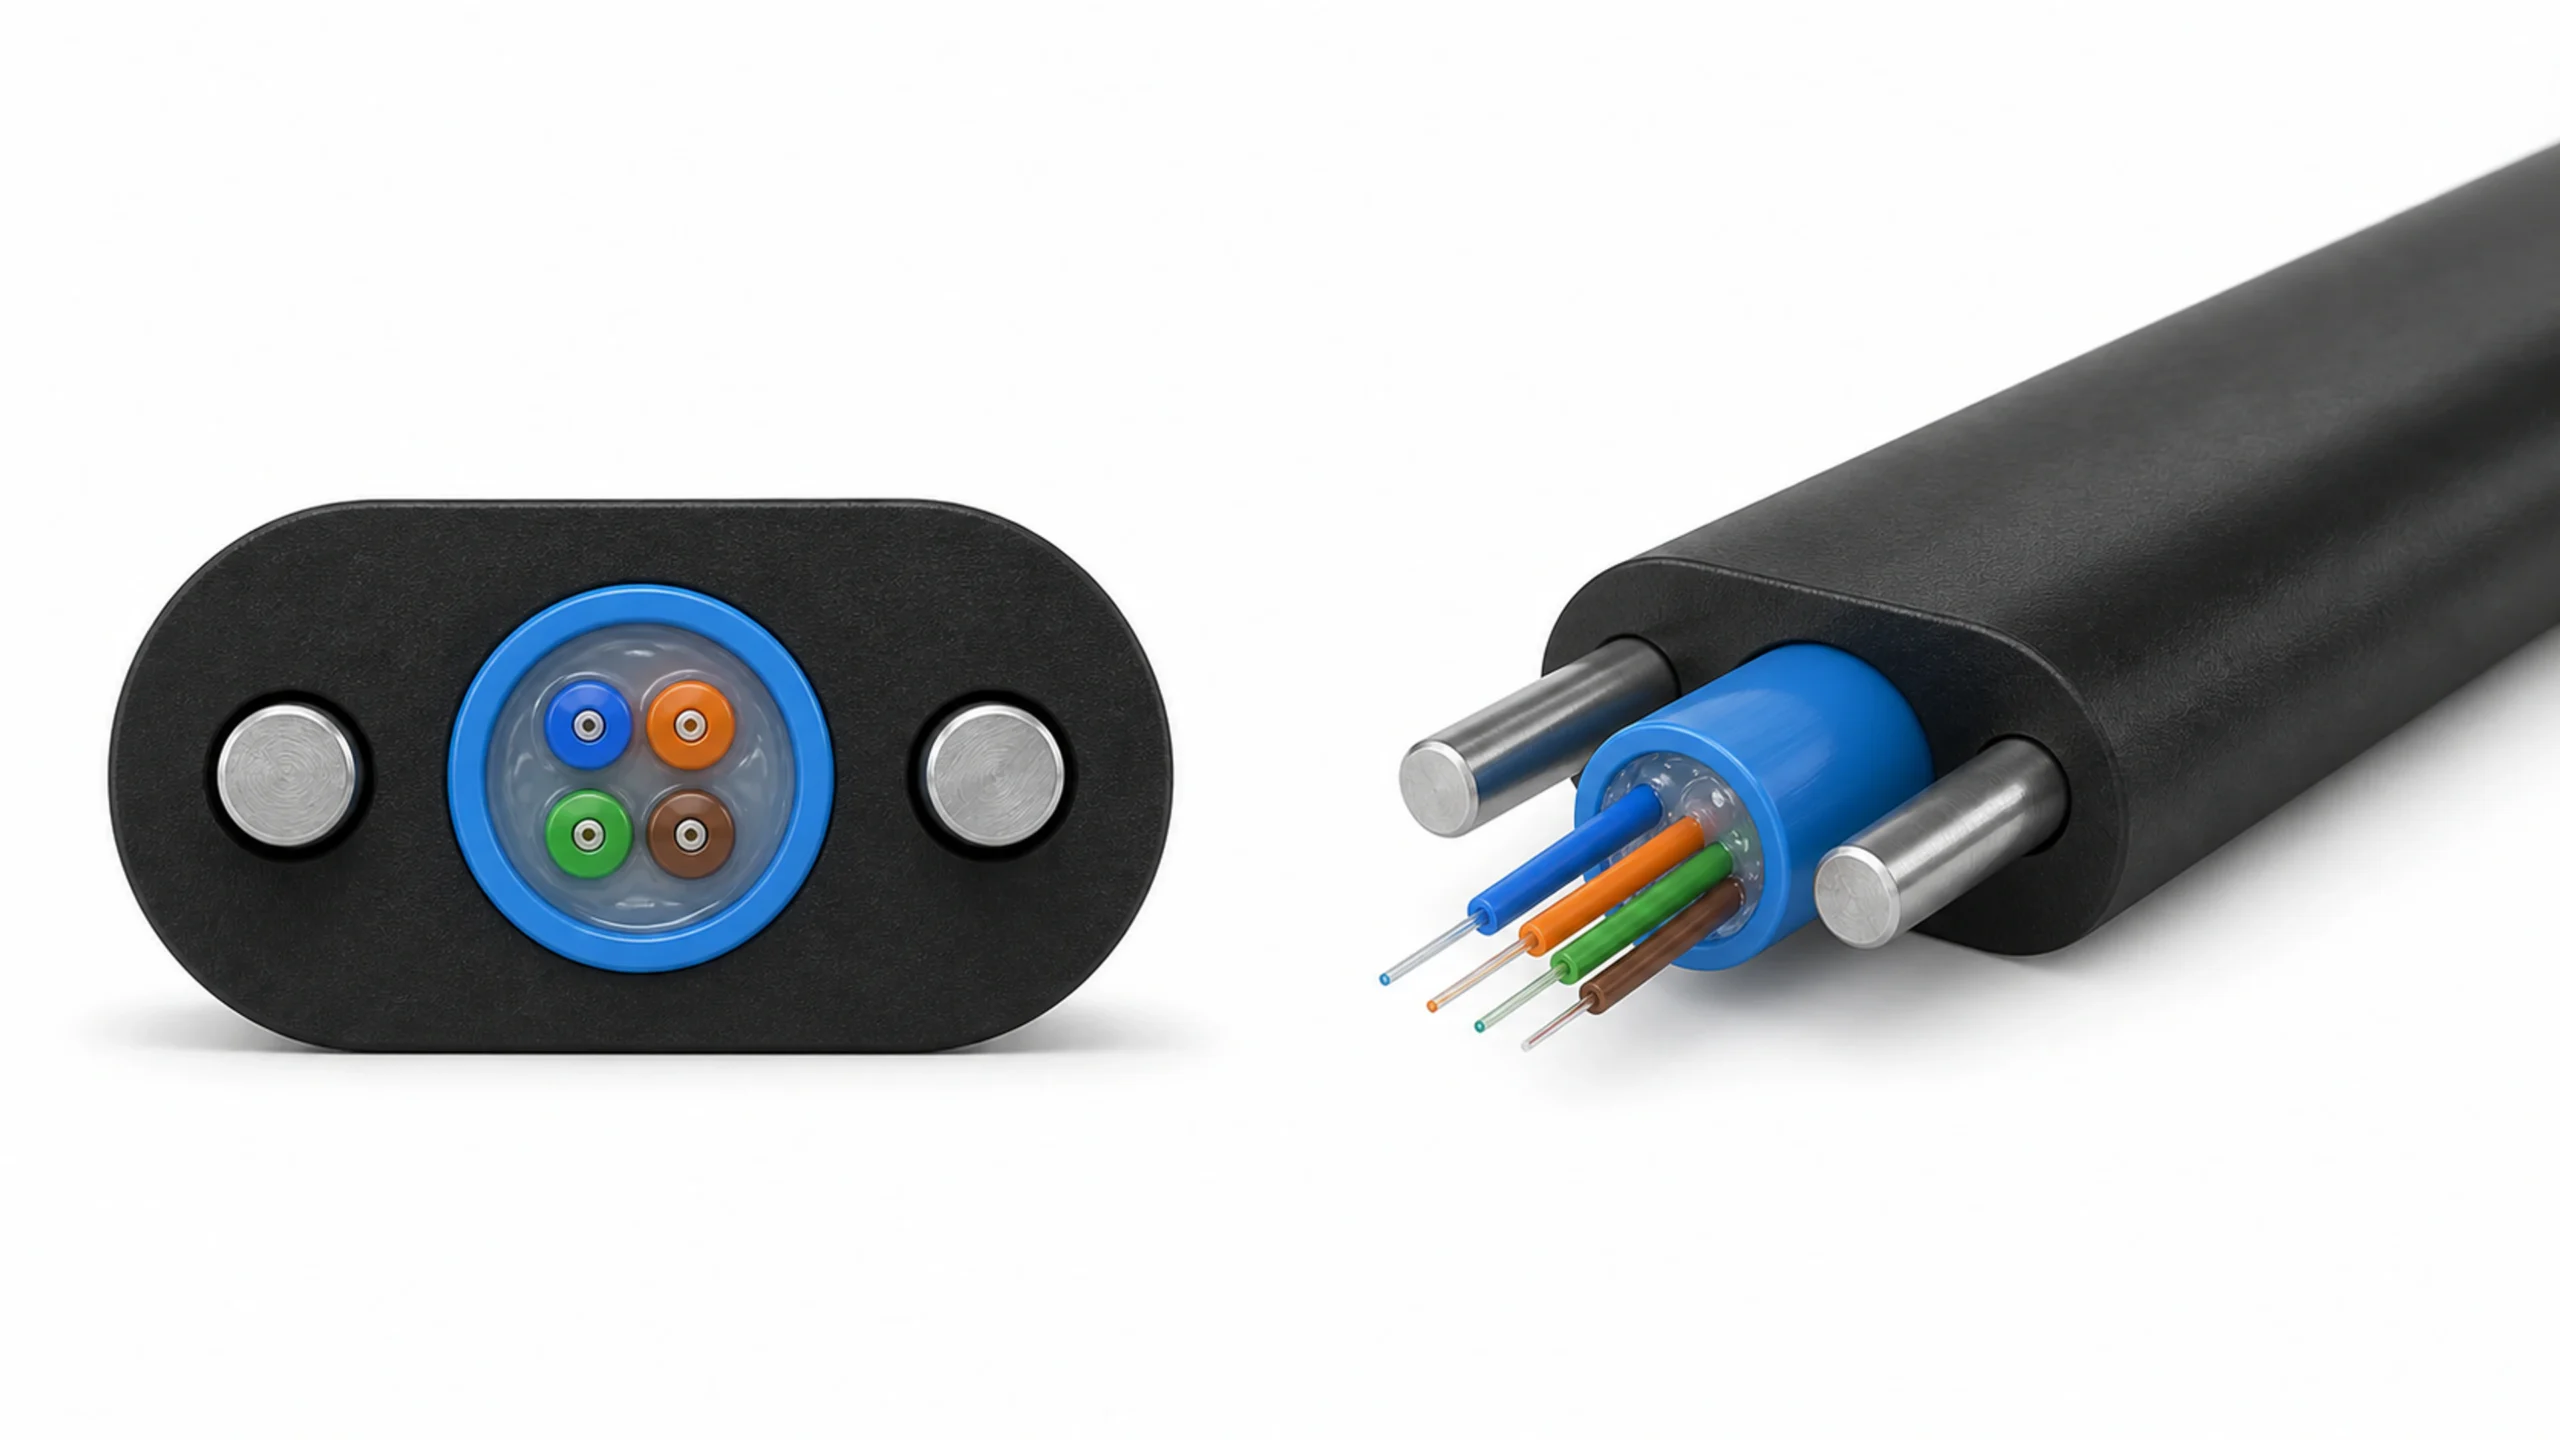
Review the published construction, armoring, messenger positioning and figure-8 crosshead tooling together.
Open cable solutionConstruction matters: armored, all-dielectric and figure-8 cables require different preparation, reinforcement and tooling. One illustrated arrangement does not establish compatibility with every cable.
لمعالجة البثق لأنابيب، راجع الـ خط إنتاج الأنابيب السائبة. بالنسبة للنواة المجدولة، راجع الـ خط إنتاج التضفير SZ.
The HONGKAI HK-90 video shows a sheathing reference for an ADSS cable route. Use it to discuss equipment and operating sequence, then agree the trial for your construction.
استخدم القلب المعتمد، ومركب الغلاف، ومواد الحماية وبكرة الخرج.
Observe extrusion, cooling, diameter monitoring, traction and take-up during starts, steady running and stops.
Check finished diameter, sheath thickness and appearance, marking, winding and the agreed optical and jacket tests.
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
ابدأ برسمك أو متطلبات منتجك أو المعدات الحالية. يمكن تأكيد التفاصيل الفنية خلال المراجعة الأولى.
Cable drawing and finished dimensions
Incoming core or loose-tube details
Sheath compound and jacket thickness
Reinforcement, tape and ripcord requirements
Input and output drum sizes / weights
Target output and operating plan
Marking, testing and acceptance criteria
تخطيط المصنع والمعدات المحتفظ بها
Utilities, installation and project timing
Review the cable construction, equipment boundary and information needed for a proposal.
تقوم بتطبيق الغلاف الخارجي المحدد على قلب كابل بصري مُحضَّر أو على أنبوب خاص بالبناء وحزمة الحماية، ثم تبرّد الكابل وتفحصه وتجمعه. إن عمليات تلوين الألياف المنبعية، والبثق لأنبوب غير مشدود، والتضفير الحلزوني (SZ) هي مراحل منفصلة ما لم تُدرَج ضمن نطاق المشروع.
يمكن أن تتضمن عائلات الكابلات هذه مرحلة تغليف HK-90، لكنها لا تستخدم مجموعة معدات متطابقة. يجب مراجعة التعامل مع القلب، والتعزيز، والدرع، ووضعية الحبل الناقل، وأدوات الرأس المتقاطع، والاختبارات اللاحقة لكل رسم كابل.
لا. يتم اختيار آلات إخراج الشريط المعدني، والربط، والتراكم، والتموج، والتشكيل الطولي للبناء المدرع أو ذي الغلاف المركب المحدد. يتطلب المسار العازل بالكامل متطلبات تدعيم مختلفة.
The reference ratings are up to 80 m/min for PE cable below 10 mm and an extrusion-output reference of up to 250 kg/h PE with the crosshead open. These values describe stated reference conditions. Actual accepted cable output must be agreed for the cable, compound, tooling, cooling and operating plan.
يصف مرجع البثق المزوَّد مادتي البولي إيثيلين (PE) والبولي فينيل كلورايد (PVC). يُرجى تأكيد الدرجة الدقيقة والمسمار المطلوب، والأدوات، وإعدادات التجفيف ودرجة الحرارة. لا تفترض أن مركب LSZH أو أي مركب آخر مشمول دون مراجعة هندسية منفصلة.
يتضمن مرجع المعدات جهاز تجميع الشريط المعدني، الذي يخزن الشريط لاستخدامه في تسلسل وصله. ويؤدي جهاز تجميع الكابل النهائي وظيفة مختلفة ويتطلب إعداداته الخاصة ومراجعة خاصة به فيما يتعلق بالتوتر وطول التخزين وتغيير البكرة.
يعتمد تطبيق الاختبار على تركيب الكابل ووجود مسار كهربائي مناسب للعودة. لا يجب تلقائيًا تعيين ترتيب اختبار الشرارة نفسه لكابل عازل بالكامل كما هو الحال مع كابل يحتوي على معدن. يُرجى تأكيد طريقة الاختبار ومعايير القبول الخاصة بالمنتج الفعلي.
أرسل رسم الكابل، واللب الوارد، ومادة الغلاف، ومواد الحماية، وأحجام البكرات المطلوبة، وهدف الإنتاج. أضف مخطط مصنعك والماكينات الموجودة لديك إن توفرت. يمكن استكمال التفاصيل الفنية أثناء المراجعة الأولى.