Ekstrusi Φ90 mm · Pay-off inti hingga take-up kabel jadi
USD 118,900 per set
Konfigurasi yang ditawarkan: HK-90 PLC+IPC Kontrol Lantai Produksi Pelapisan Kabel Optik Luar Ruangan. Pengiriman dari pabrik; pembeli mengatur dan membayar transportasi. Peralatan akhir dan perkakas mengikuti jadwal konfigurasi yang telah disepakati.
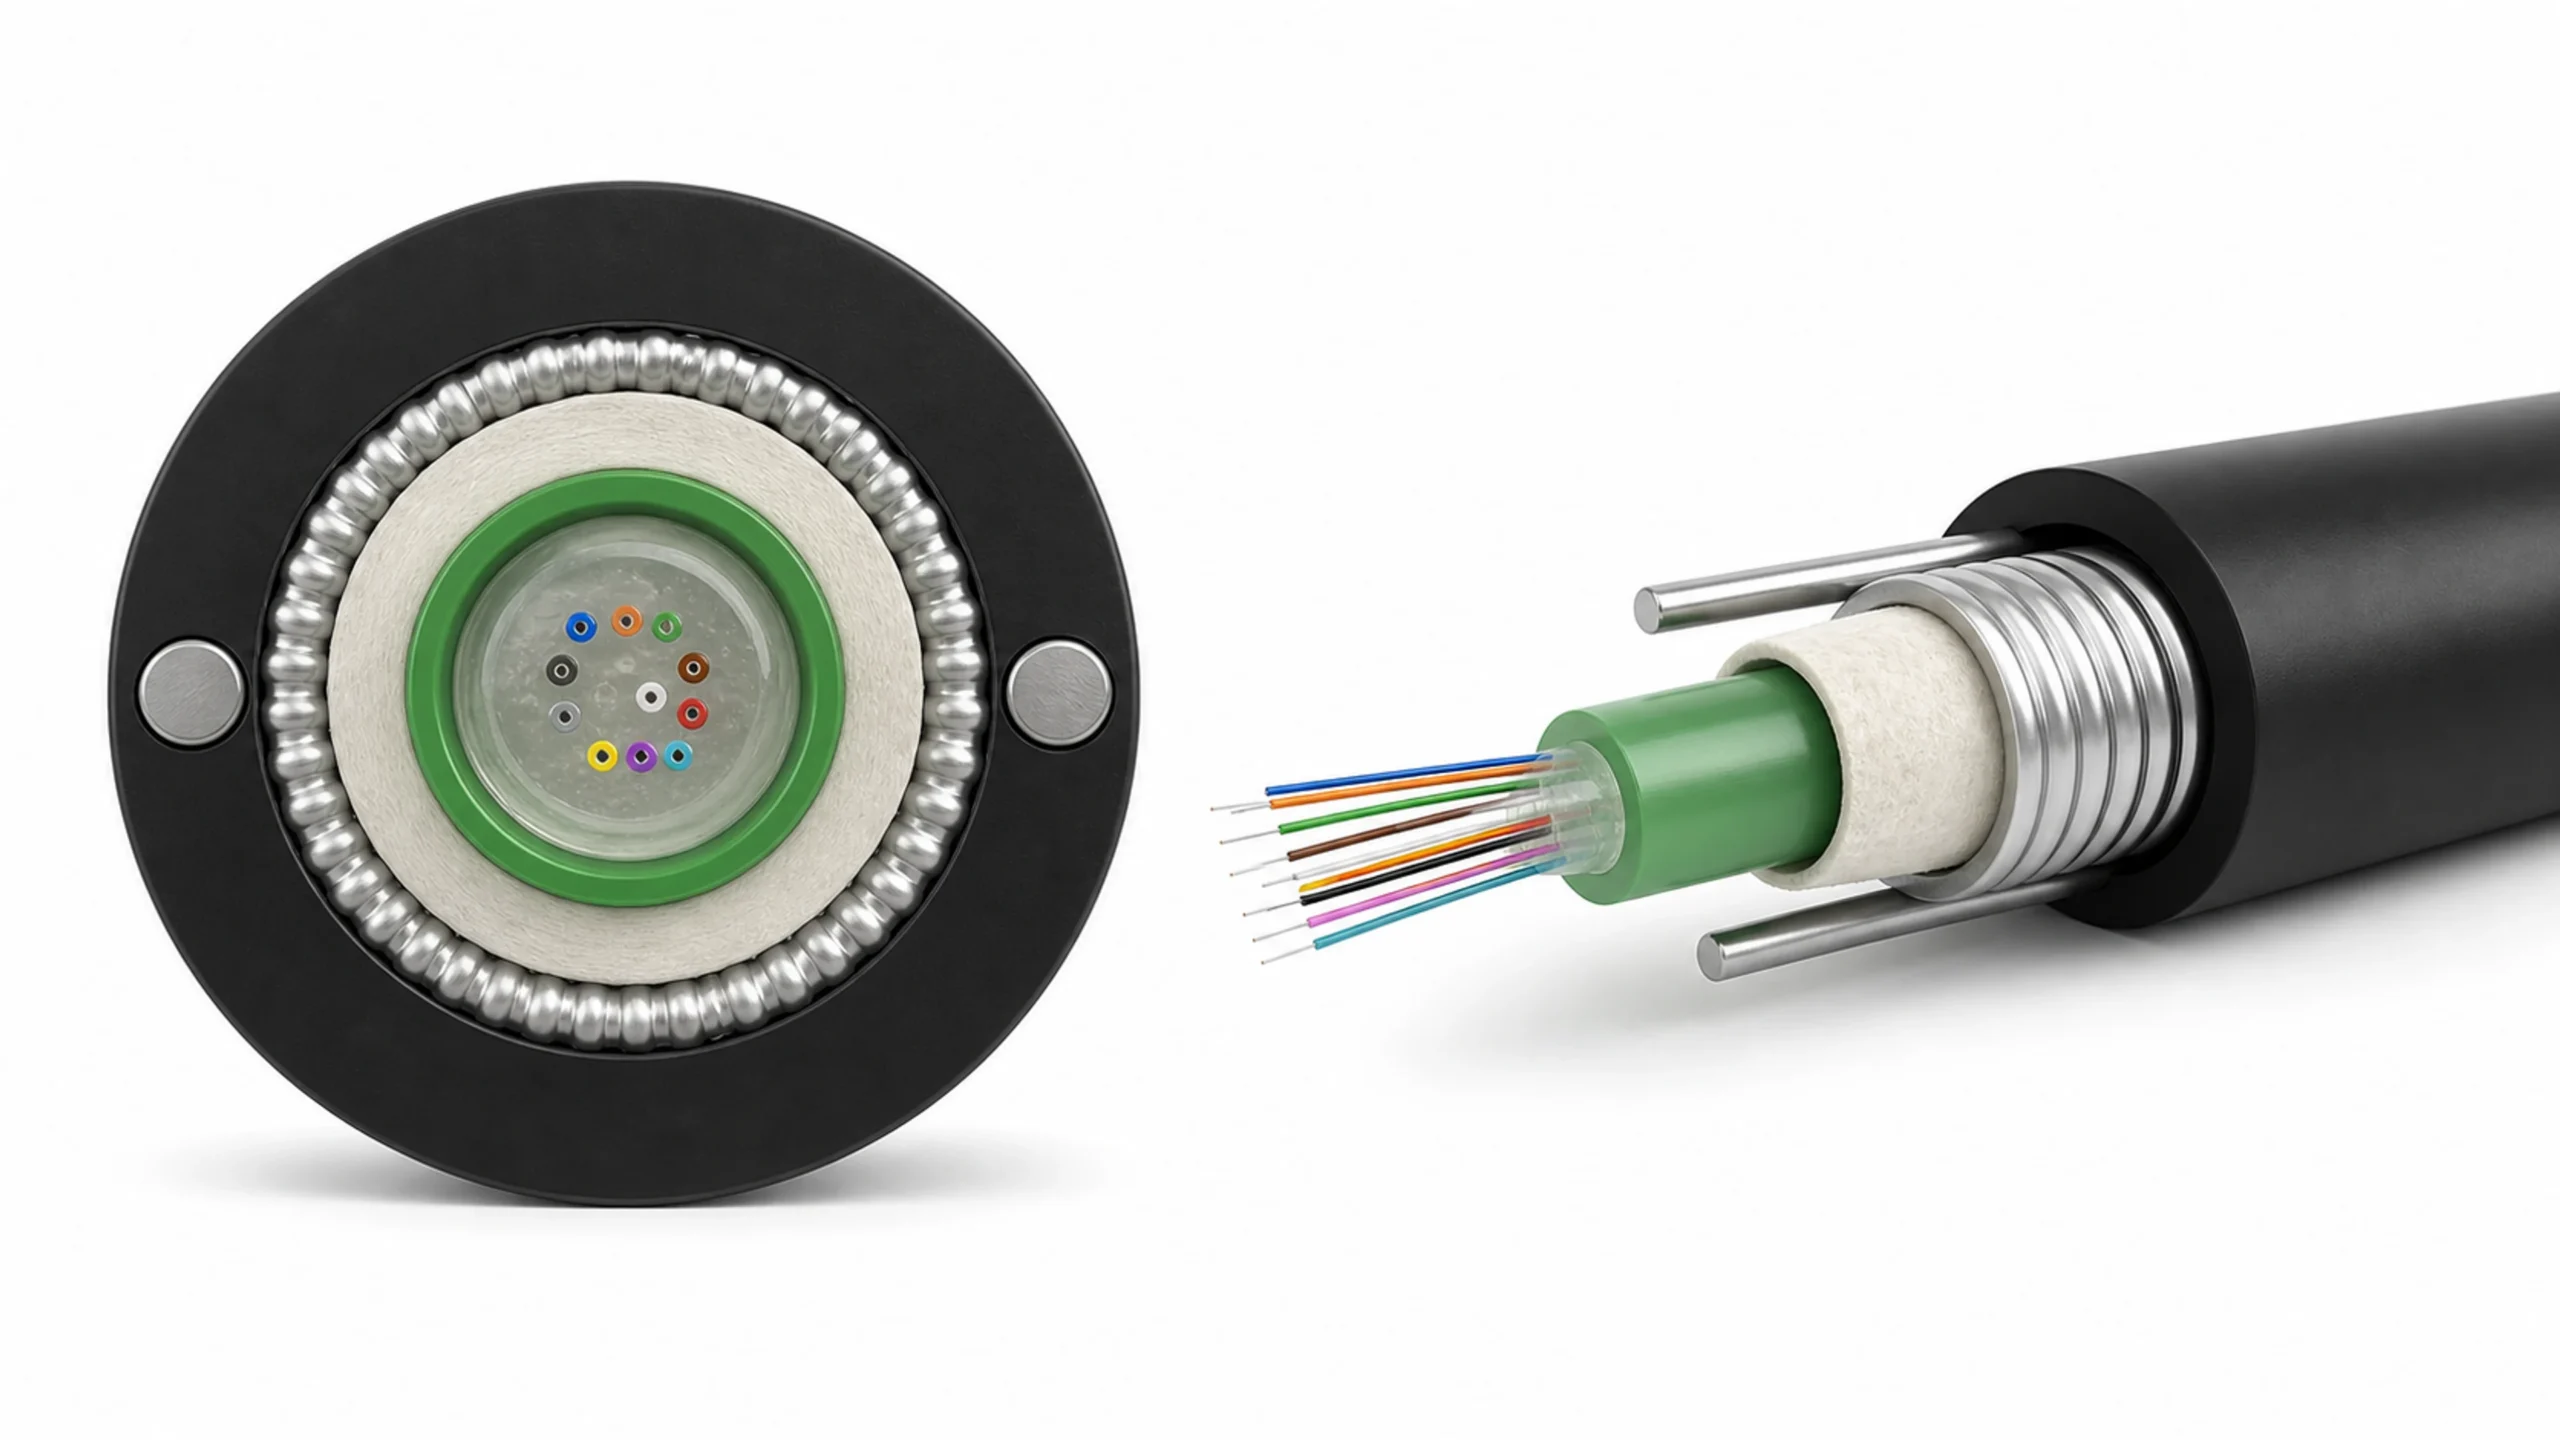
Apply the specified outer sheath around your prepared optical cable core. Configure material feeding, aramid yarn stranding or metal-tape protection as required, extrusion, cooling and take-up as one coordinated production stage.
Coordinate melt delivery, tooling, cooling and traction around the cable design.
REFERENCE ARRANGEMENTEquipment quantities and final layout follow the reviewed project.
Scope boundary: this page covers the sheathing stage. Upstream coloring, loose-tube extrusion and SZ core stranding are separate processes. Reinforcement and armoring modules are selected for the approved cable construction.
02PROCESS & MATERIAL HANDOFF
From prepared core to finished outer sheath.
Build the process around the cable layers. Optional protection modules are selected before the extrusion and downstream handling requirements are finalized.
01CORE & MATERIAL PAY-OFF
Feed the specified construction.
Start with the prepared core or loose tube. Match the core, wire and protection-material pay-offs to the incoming package.
02PROTECTION & FORMING
Prepare the layers before extrusion.
Apply the selected water blocking and ripcord. ADSS routes add aramid yarn stranding before the outer sheath; armored routes use the specified metal-tape preparation and forming modules.
03SHEATH EXTRUSION
Form the outer jacket.
Feed the approved compound to the Φ90 mm extruder and crosshead. Coordinate melt delivery, cable centering, temperature and line speed.
04COOLING TO TAKE-UP
Cool, inspect and collect.
Cool and dry the sheath, monitor diameter, apply the specified marking and tests, then coordinate caterpillar traction with finished-cable take-up.
3DINTERACTIVE LINE VIEW
Explore the line. Inspect each device.
Rotate the HK-90 line, select a device for a closer look, and compare its exterior with the original equipment photograph.
Preparing the interactive line…
The interactive view could not finish loading. Retry the 3D view, or use the equipment references on this page.
Illustrative exterior study. Final equipment, dimensions and layout follow the approved project configuration.
03CONFIGURATION & PROJECT SCOPE
Choose the protection route for your cable.
The same extrusion stage can sit within different process routes. Compare the incoming core, reinforcement and tape requirements before defining the equipment package.
CONFIGURATION BASISModul khusus konstruksi · lingkup akhir berdasarkan gambar kabel
04EQUIPMENT IN THE LINE
Follow the line, one machine at a time.
Select a number or equipment card to see its equipment area, image and process role. Dashed regions identify process interfaces whose final position must be confirmed. The reference includes optional preparation and testing modules; the final equipment list follows your cable construction.
HK-90 EQUIPMENT MAP · REFERENCE ARRANGEMENT
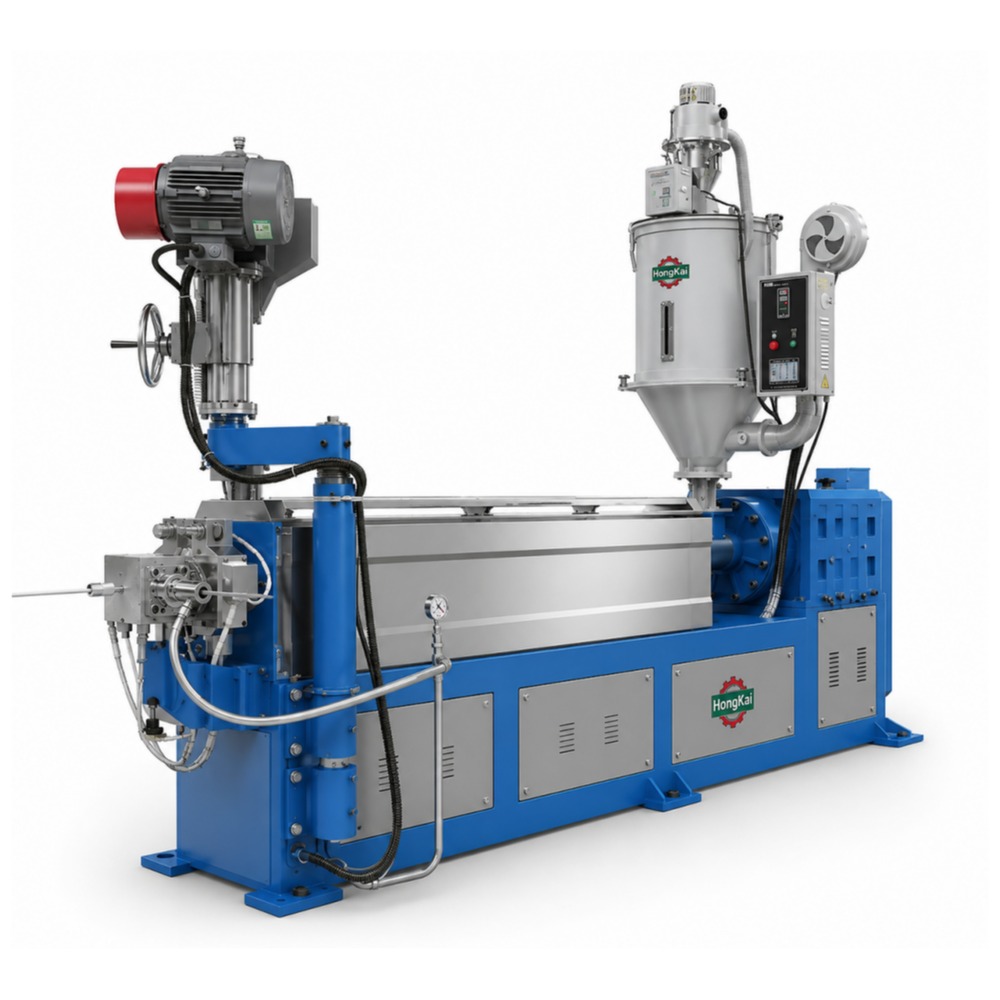
13 Bahasa Indonesia: Φ90 mm sheath extruderEquipment area in the reference arrangement
SELECTED EQUIPMENT · PROJECT REFERENCE13 / 23
Equipment shown is for reference. Final construction and quantity follow your approved equipment list.
SHEATH EXTRUSION
Φ90 mm sheath extruder
Plasticizes the approved sheath compound and supplies the adjustable crosshead. The reference uses a Φ90 mm screw with a 25:1 L/D ratio.
CONFIRM FOR YOUR PROJECT
Compound grade, screw and crosshead, tooling, temperature profile, output and required jacket dimensions.
Selected equipment 13: Φ90 mm sheath extruder
Referensi batas: the panorama illustrates equipment order, not the final machine count, footprint or construction. The approved layout and equipment list define machine quantities, dimensions and the supplied arrangement.
05TECHNICAL CONFIGURATION REVIEW
Tentukan kondisi operasional di balik spesifikasi tersebut.
Gunakan referensi di bawah ini untuk memulai tinjauan teknis. Konfirmasi konstruksi kabel lengkap, tingkat mutu material, dan kondisi uji coba sebelum menyetujui kinerja produksi.
HK-90 reference data and project confirmation points
Review area
Reference / requirement
Kondisi untuk dikonfirmasi
Extruder reference
Φ90 mm screw · 25:1 L/D · 75 kW main drive.
Konfigurasi peralatan referensi; sekrup, crosshead, dan perkakas harus sesuai dengan kompon dan kabel.
Referensi penggulungan Aramid
24 heads · independent tension · adjustable pitch · S or Z lay.
Selected for the cable construction. Confirm yarn grade, quantity, tension and stranding pitch together with extrusion speed. The reference 120 rpm rotation is not a cable line speed.
Sheath materials
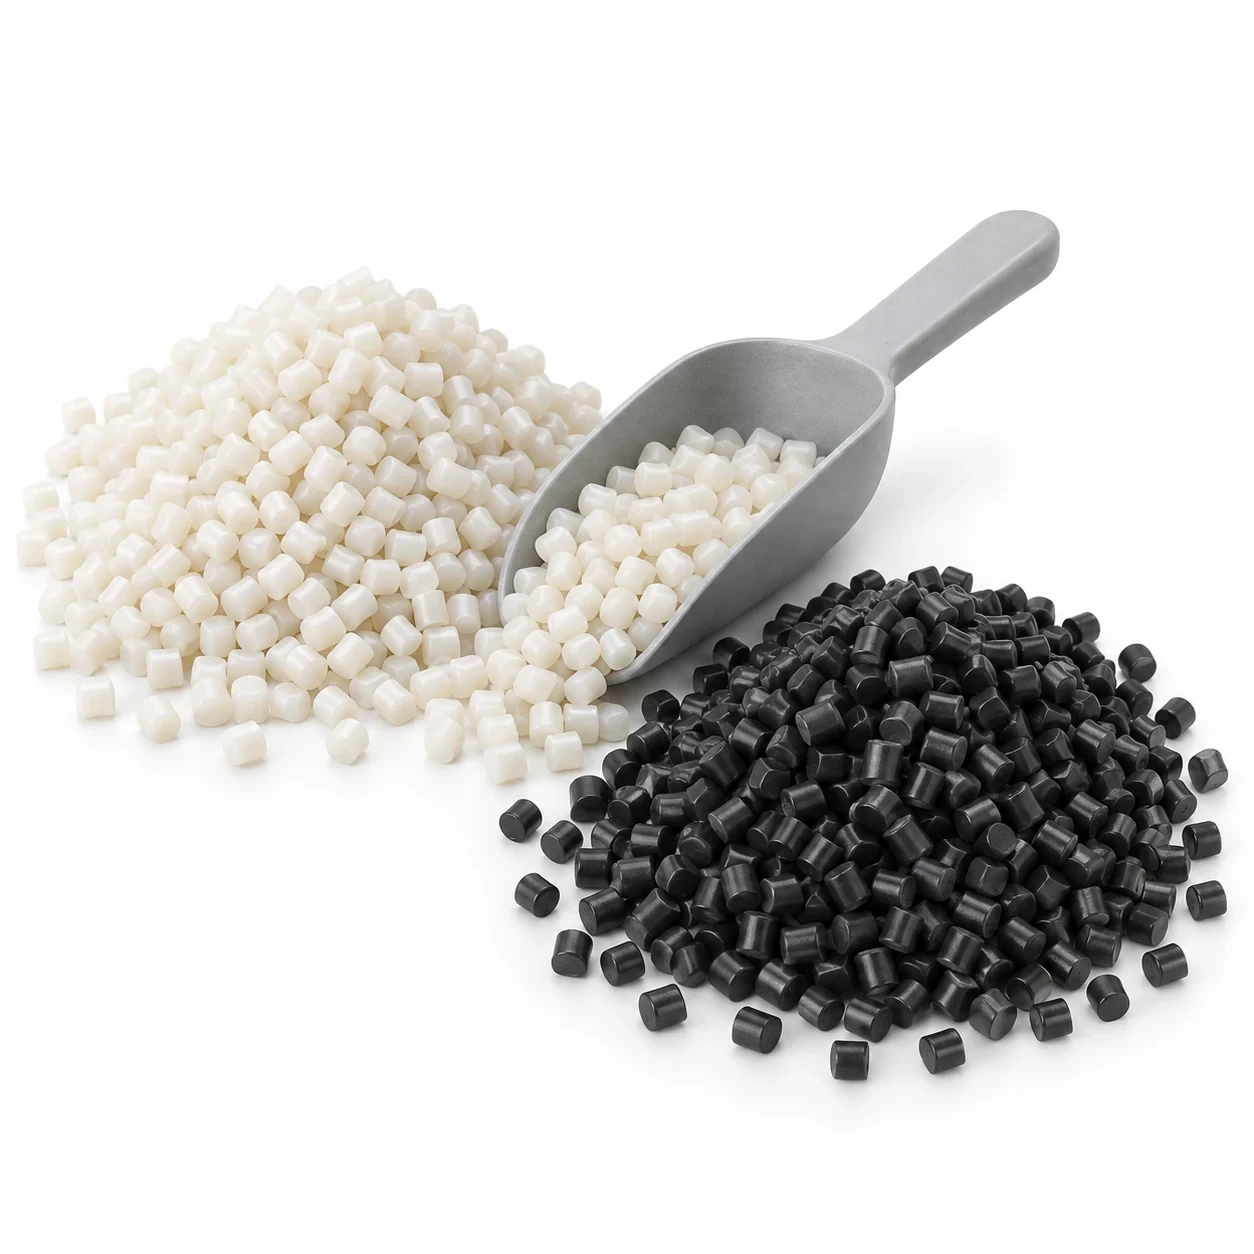
PE / PVC for the reference extruder configuration.
Confirm the compound grade and process settings. Other compounds require a separate suitability review.
Kecepatan produksi
Reference: up to 80 m/min for PE cable below Φ10 mm.
Reference value; confirm the complete construction, jacket thickness, cooling, reel changes and quality targets.
Extrusion output
Reference: up to 250 kg/h PE, with the crosshead open.
An extruder-output reference is not guaranteed finished-cable throughput. Verify it with the agreed tooling and compound.
Cable & tooling range
Specify incoming core, finished diameter and jacket thickness.
Review every module. A metal-tape forming tool may have a narrower range than the extruder or capstan.
Reels, tension & utilities
Agree supply/output drums, winding tension, layout and utility loads.
Use one approved schedule for the chosen configuration; do not infer these values from the HK-90 name.
Controls & acceptance
PLC / IPC coordination, recipes, alarms and agreed inspection records.
Define instruments, interfaces, safety functions, trial duration and acceptance criteria.
CABLE DRAWING → TECHNICAL SCHEDULE → ACCEPTANCE
Konfirmasi jadwal teknis untuk kabel Anda.
Review output together with the sheath cross-section, compound, tooling and cooling capacity. Reel capacity, line footprint, tension settings and utility loads are finalized for the selected configuration.
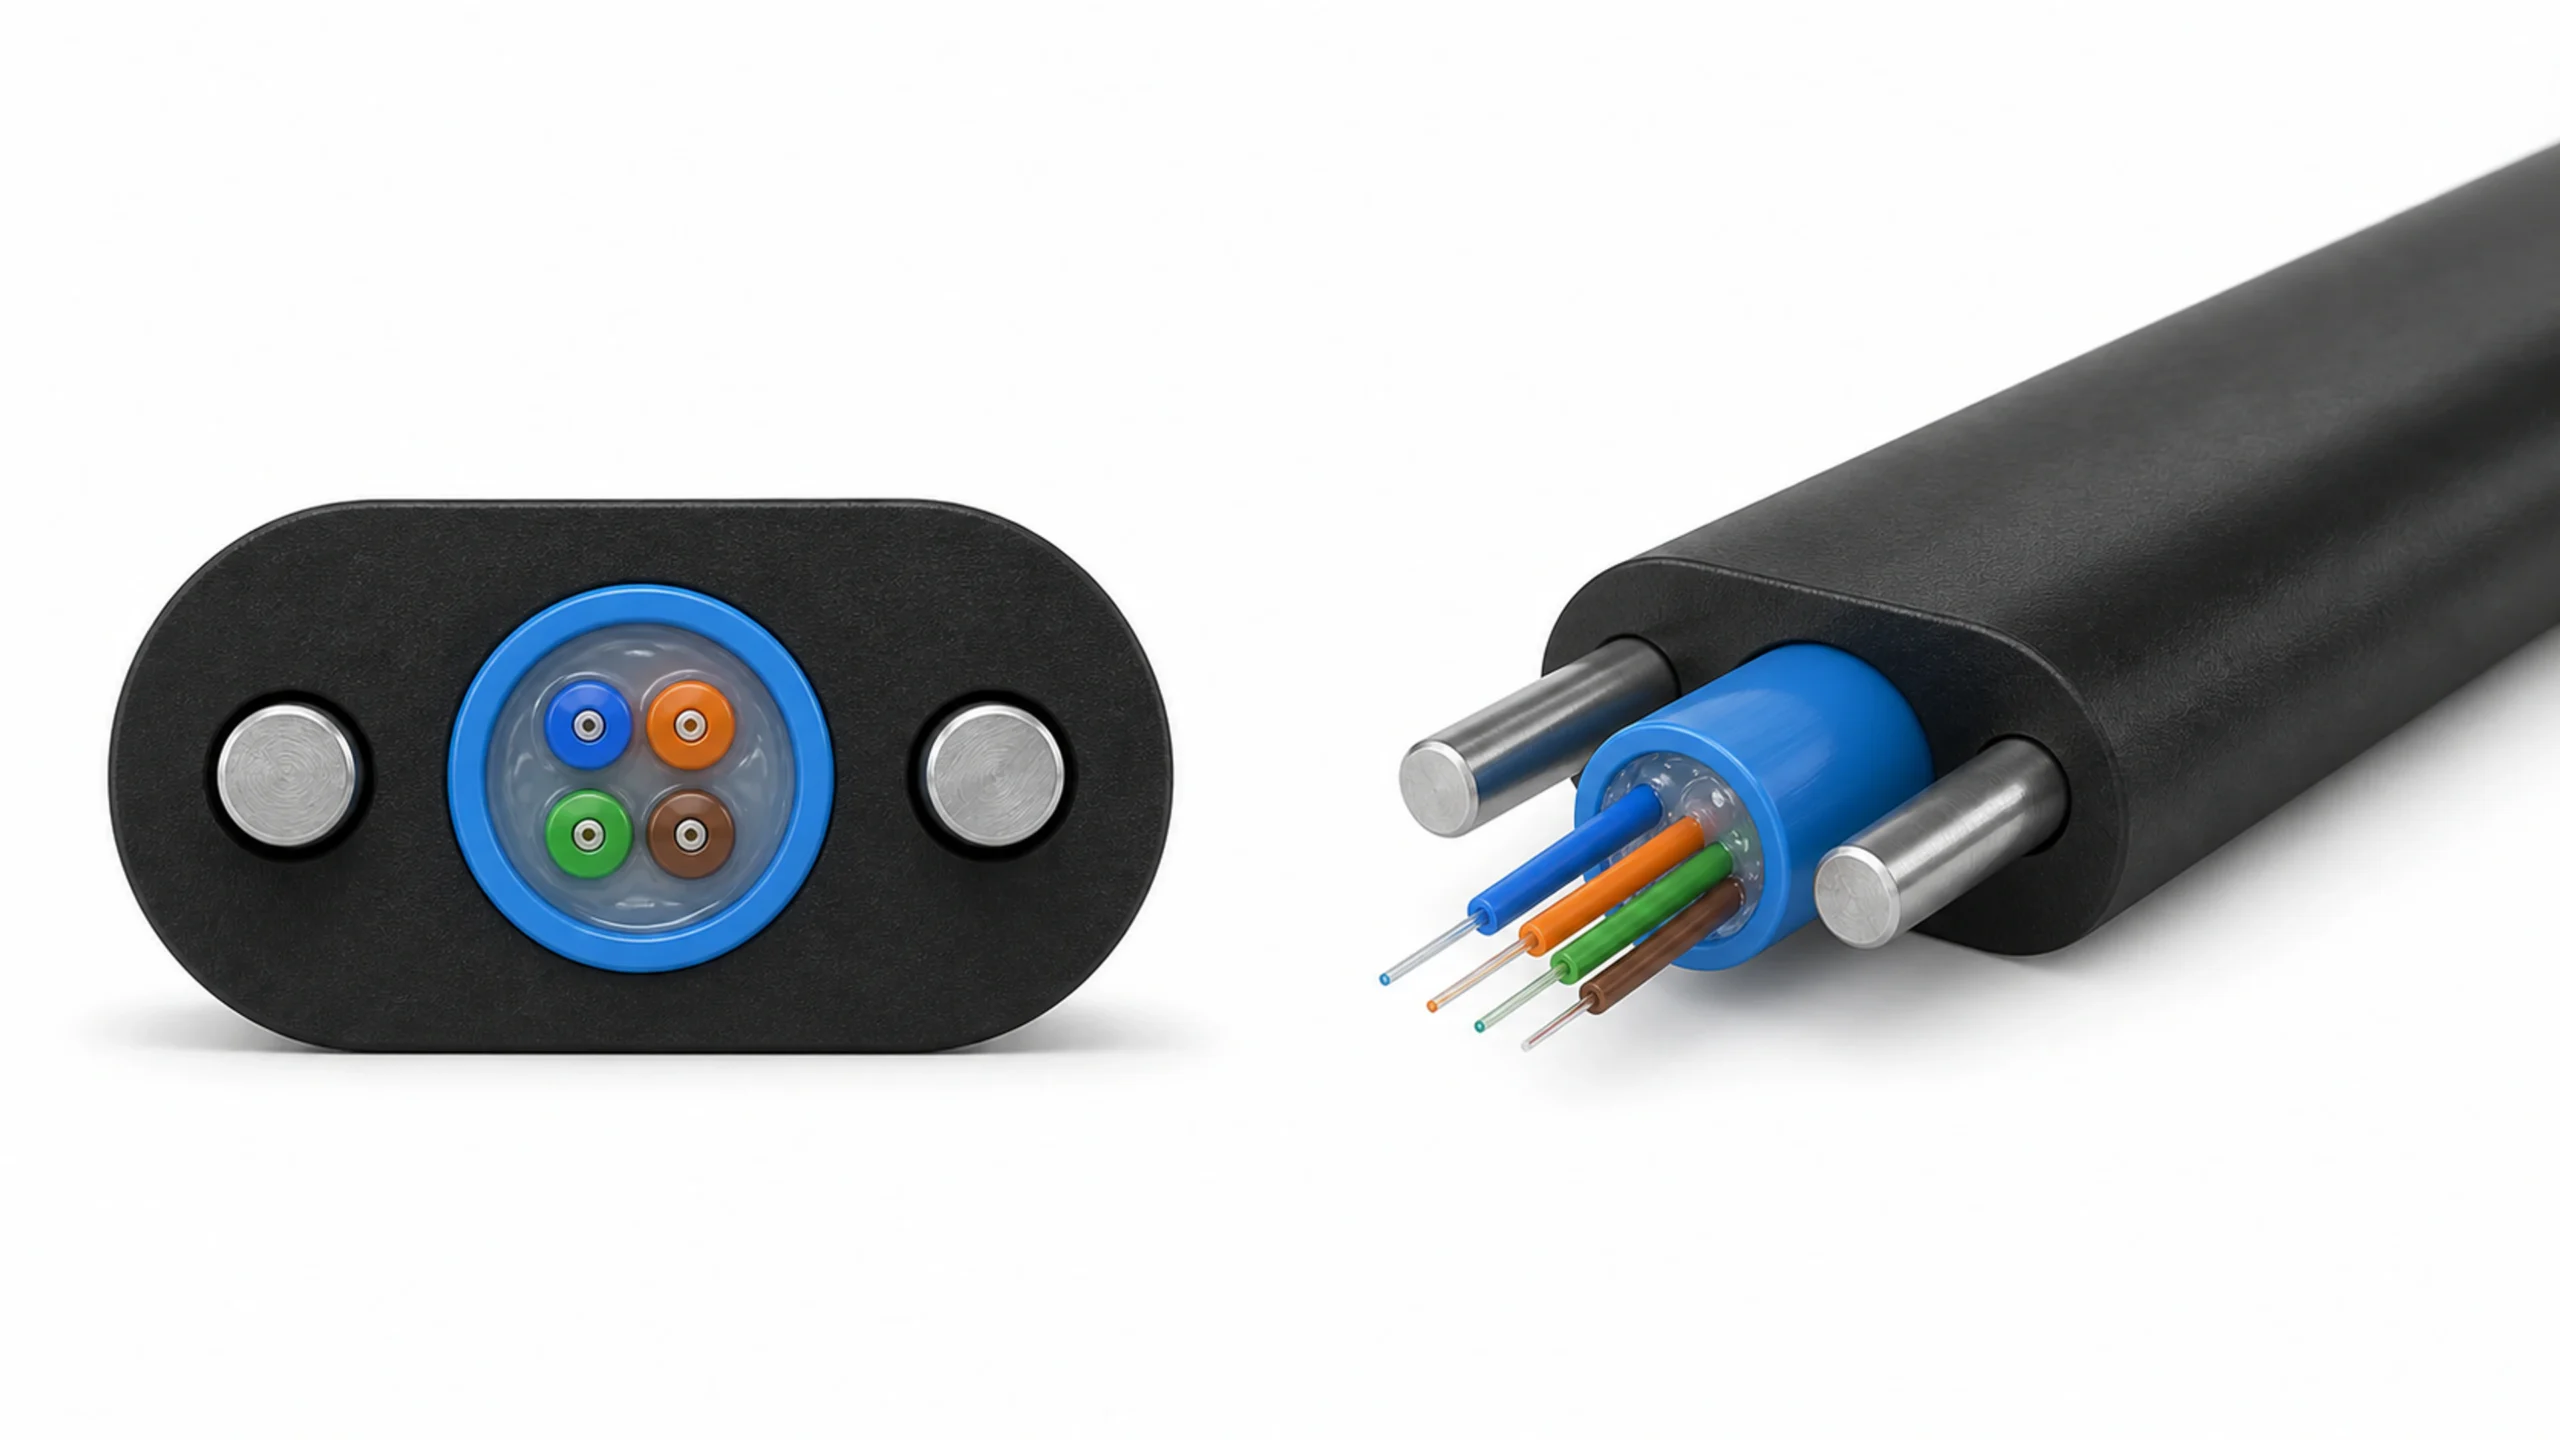
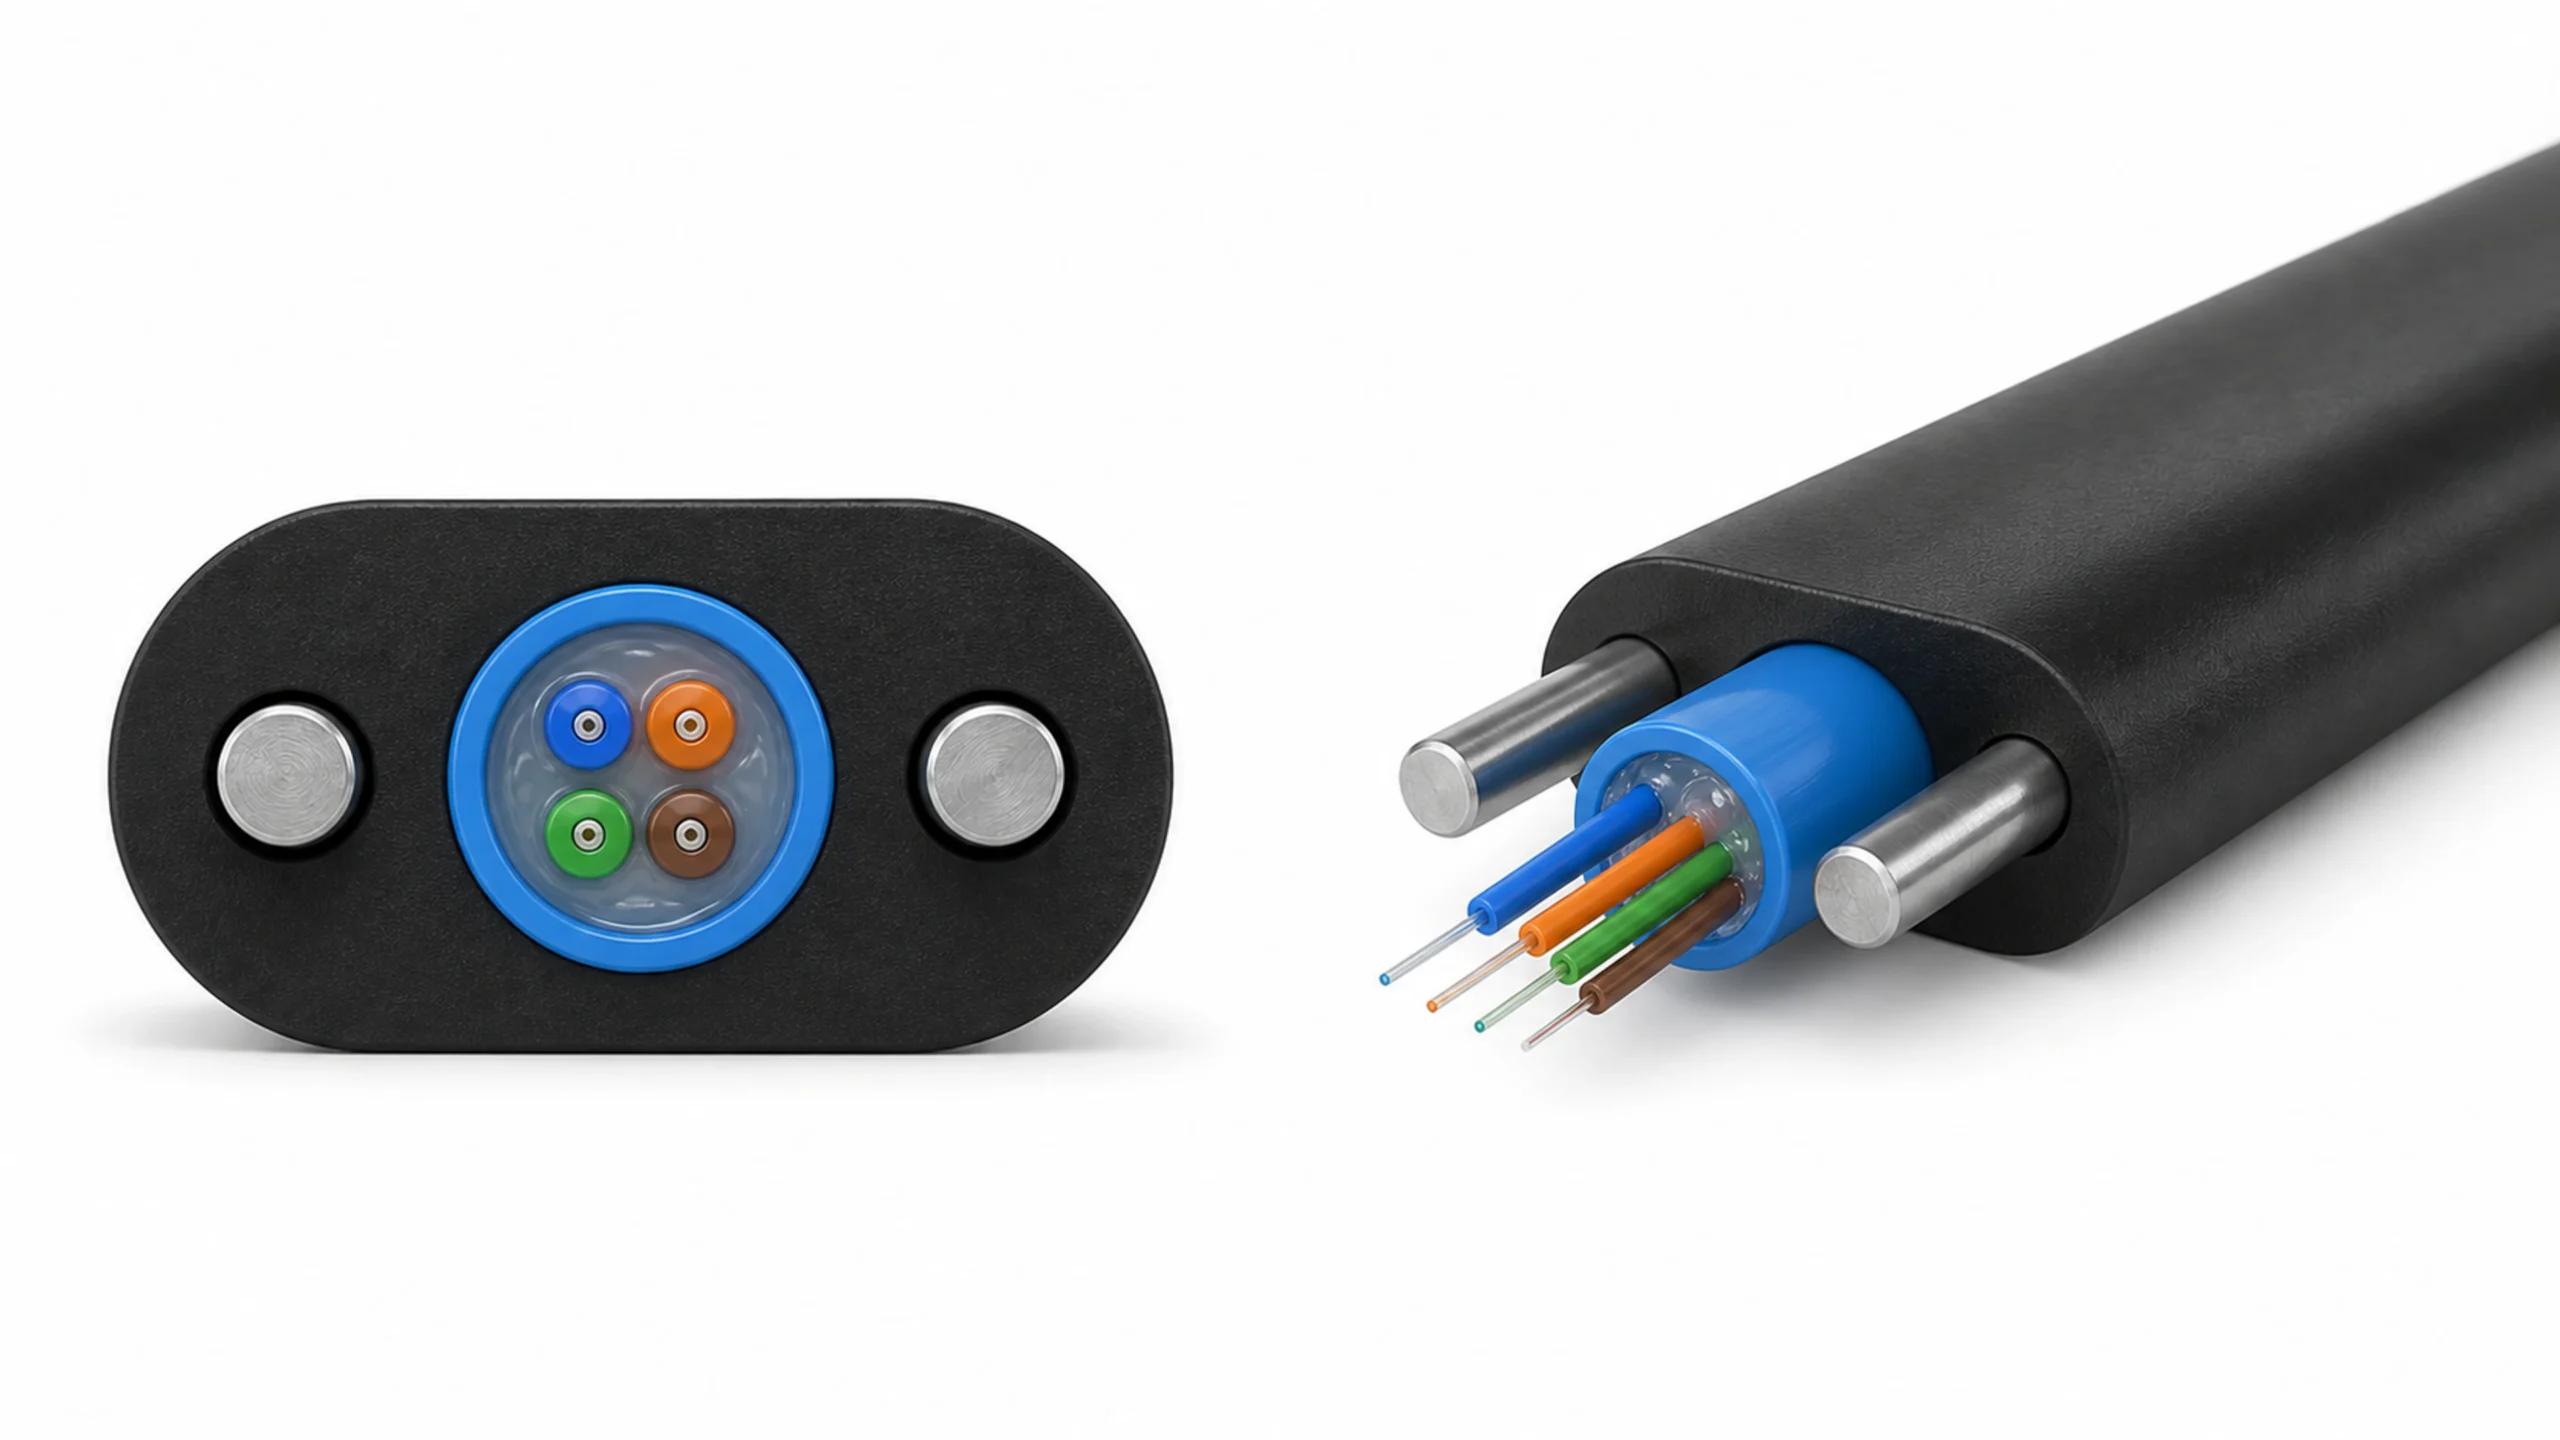
Construction matters: armored, all-dielectric and figure-8 cables require different preparation, reinforcement and tooling. One illustrated arrangement does not establish compatibility with every cable.
See the sheathing process. Plan the acceptance trial.
The HONGKAI HK-90 video shows a sheathing reference for an ADSS cable route. Use it to discuss equipment and operating sequence, then agree the trial for your construction.
01PRODUCT
Cobalah konstruksi yang ditentukan.
Gunakan inti yang telah disetujui, senyawa selubung, bahan pelindung, dan drum keluaran.
02PROCESS
Periksa perilaku terkoordinasi.
Observe extrusion, cooling, diameter monitoring, traction and take-up during starts, steady running and stops.
03OUTPUT
Agree the inspection record.
Check finished diameter, sheath thickness and appearance, marking, winding and the agreed optical and jacket tests.
ACCEPTANCE BASISGambar yang disetujui + material yang disepakati + kondisi operasi + metode inspeksi tertulis
Hubungkan pasokan peralatan dengan start-up pabrik.
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
01
Lingkup peralatan
Tentukan modul yang disediakan dan jumlahnya
Identifikasi peralatan yang dipertahankan dan disediakan oleh pembeli
Catat tanggung jawab sumber peralatan
02
Line integration
Tinjau tata letak dan antarmuka alur material
Tentukan kontrol, utilitas, dan batas keselamatan
Menyetujui ruang lingkup instalasi dan komisioning
03
Mulai & dukungan
Tentukan produk uji coba dan catatan penerimaan
Confirm operator training and documentation
Menyetujui ruang lingkup suku cadang dan purnajual
09START THE ENGINEERING REVIEW
Tell us about the cable you need to sheath.
Start with your drawing, product requirements or existing equipment. Technical details can be confirmed during the first review.
WHAT TO PREPARE
Nine inputs for your sheathing line.
01
Cable drawing and finished dimensions
02
Incoming core or loose-tube details
03
Sheath compound and jacket thickness
04
Reinforcement, tape and ripcord requirements
05
Input and output drum sizes / weights
06
Target output and operating plan
07
Marking, testing and acceptance criteria
08
Factory layout and retained equipment
09
Utilities, installation and project timing
10BUYER FAQ
Questions before specifying an HK-90 sheathing line.
Review the cable construction, equipment boundary and information needed for a proposal.
01Apa yang diproduksi oleh lini selubung HK-90?
Mesin ini menerapkan selubung luar yang ditentukan pada inti kabel optik yang telah disiapkan atau pada tabung dan paket pelindung spesifik konstruksi, kemudian mendinginkan, memeriksa, dan mengumpulkan kabel tersebut. Pewarnaan serat hulu, ekstrusi tabung longgar, dan penganyaman SZ merupakan tahapan terpisah kecuali termasuk dalam lingkup proyek.
02Dapatkah satu lini memproduksi kabel GYXTW, ADSS, dan kabel berbentuk 8?
Famili kabel ini dapat melibatkan tahap pelapisan HK-90, namun tidak menggunakan paket peralatan yang identik. Penanganan inti, penguatan, perisai, posisi messenger, perkakas crosshead, dan pengujian hilir harus ditinjau untuk setiap gambar kabel.
03Apakah setiap konfigurasi mencakup peralatan pita logam?
Tidak. Pita logam pay-off, penyambungan, akumulasi, pengkorugasi, dan pembentukan longitudinal dipilih untuk konstruksi berpelindung atau berselubung komposit yang ditentukan. Rute all-dielectric memiliki persyaratan penguatan yang berbeda.
04Apa arti kecepatan dan keluaran yang dikutip?
The reference ratings are up to 80 m/min for PE cable below 10 mm and an extrusion-output reference of up to 250 kg/h PE with the crosshead open. These values describe stated reference conditions. Actual accepted cable output must be agreed for the cable, compound, tooling, cooling and operating plan.
05Senyawa selubung mana yang dapat digunakan?
Referensi ekstruder yang disediakan menjelaskan PE dan PVC. Konfirmasi tingkat (grade) yang tepat serta pengaturan sekrup, perkakas, pengeringan, dan suhu yang diperlukan. Jangan mengasumsikan bahwa LSZH atau senyawa lainnya telah tercakup tanpa tinjauan teknis terpisah.
06Apakah akumulator kabel jadi sudah termasuk?
Referensi peralatan mencakup akumulator pita logam, yang menyimpan pita untuk rangkaian penyambungannya. Akumulator kabel jadi menjalankan tugas yang berbeda dan memerlukan konfigurasi, tegangan, panjang penyimpanan, serta tinjauan pergantian gulungan sendiri.
07Dapatkah penguji percikan jaket digunakan untuk ADSS?
Penerapan pengujian bergantung pada konstruksi kabel dan adanya jalur balik listrik yang sesuai. Kabel dielektrik penuh tidak boleh secara otomatis diberikan susunan uji percikan yang sama dengan kabel yang mengandung logam. Konfirmasikan metode pengujian dan kriteria penerimaan untuk produk aktual.
08Apa yang harus saya kirim untuk permintaan penawaran?
Kirim gambar kabel, inti masuk, senyawa selubung, material pelindung, ukuran drum yang dibutuhkan, dan target produksi. Tambahkan tata letak pabrik dan mesin yang ada jika tersedia. Detail teknis dapat dilengkapi selama tinjauan pertama.
We've detected you might be speaking a different language. Do you want to change to:





 English
 हिन्दी
 فارسی