Cable release
Manufacture and release the MPO base cable.
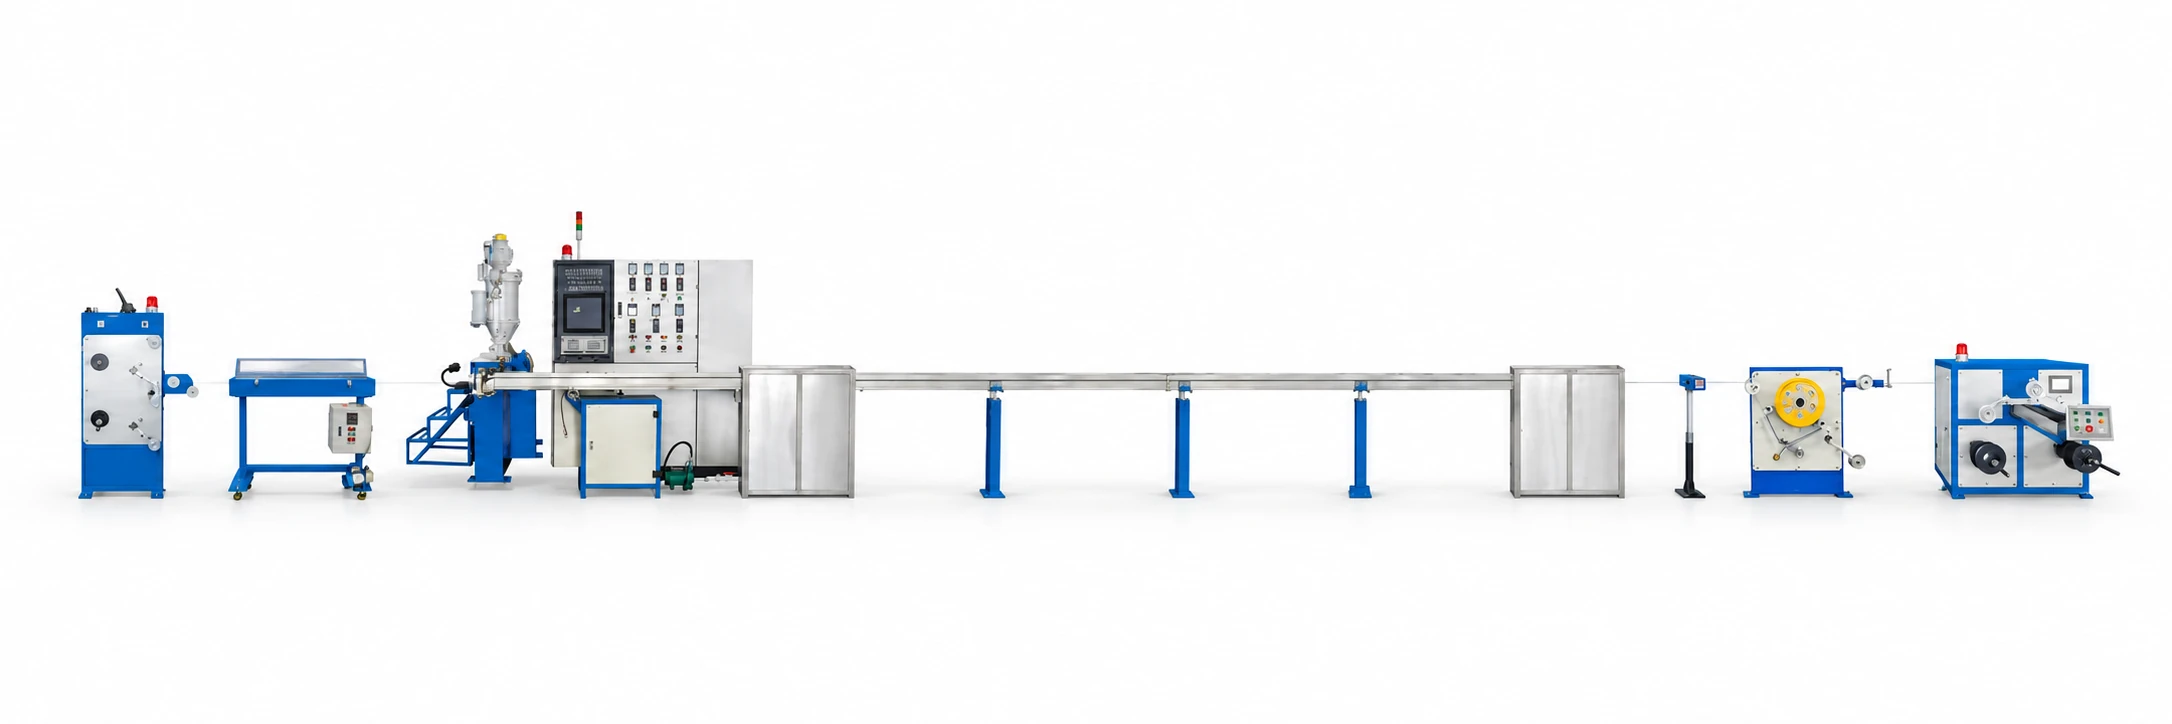
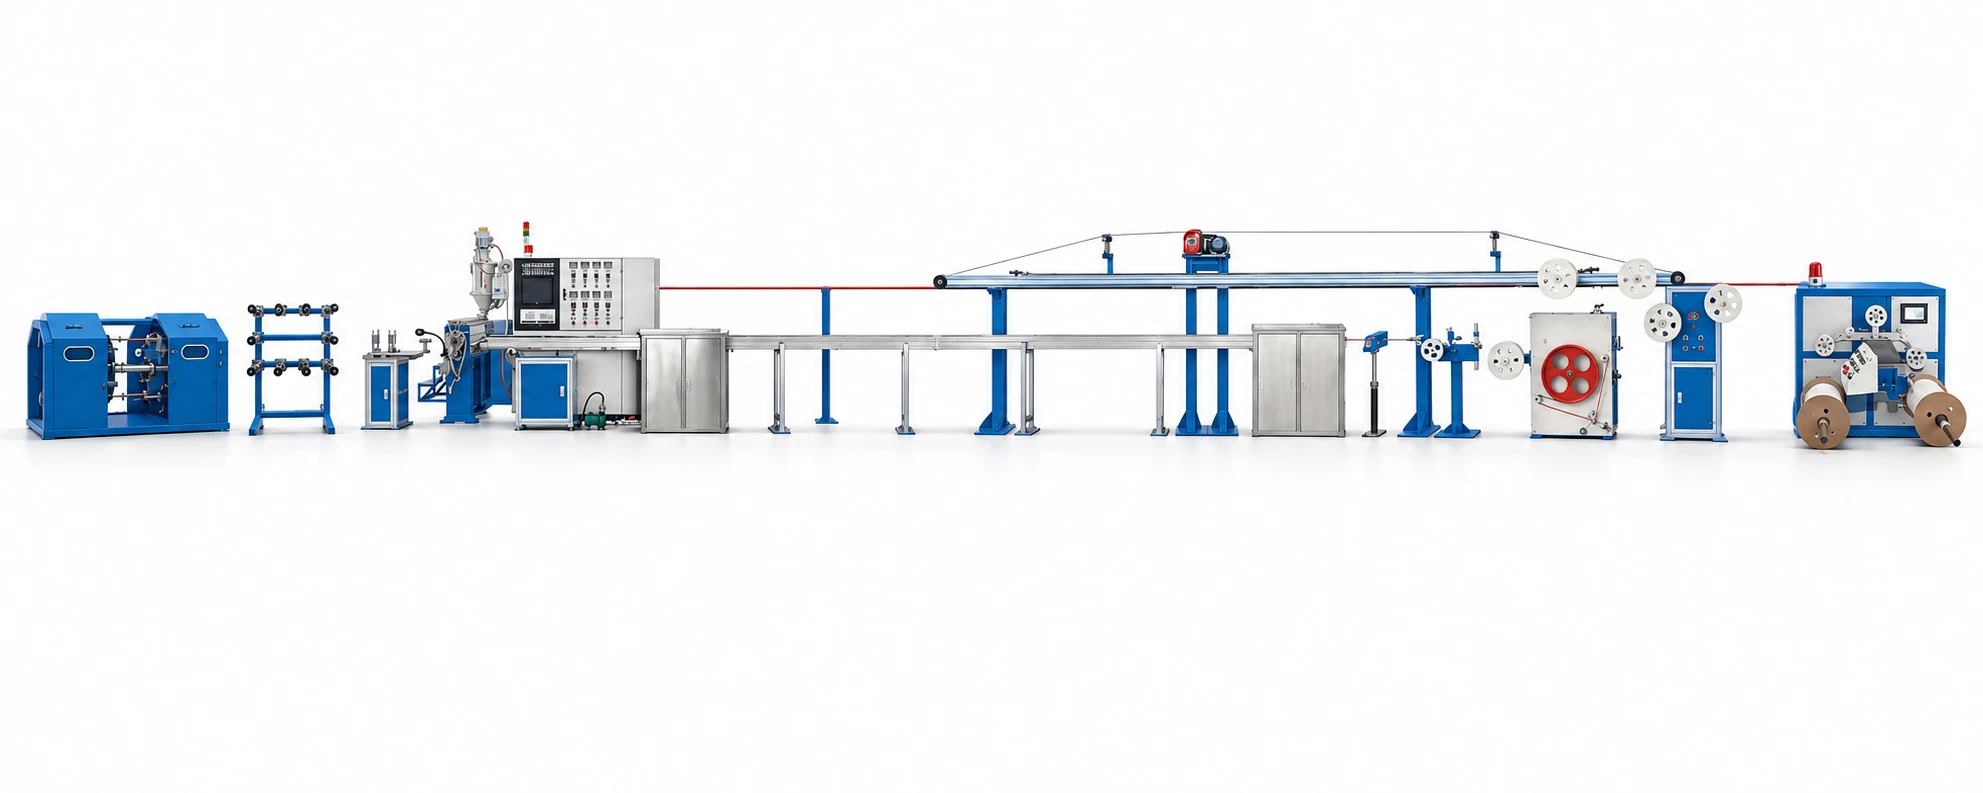
- HK-30 buffering and configured GJFJV jacketing
- Struktur kabel, dimensi, dan identifikasi serat telah diverifikasi
- Catatan rilis optik dan mekanis yang disepakati
MESIN KABEL
Peralatan untuk pembuatan kabel optik
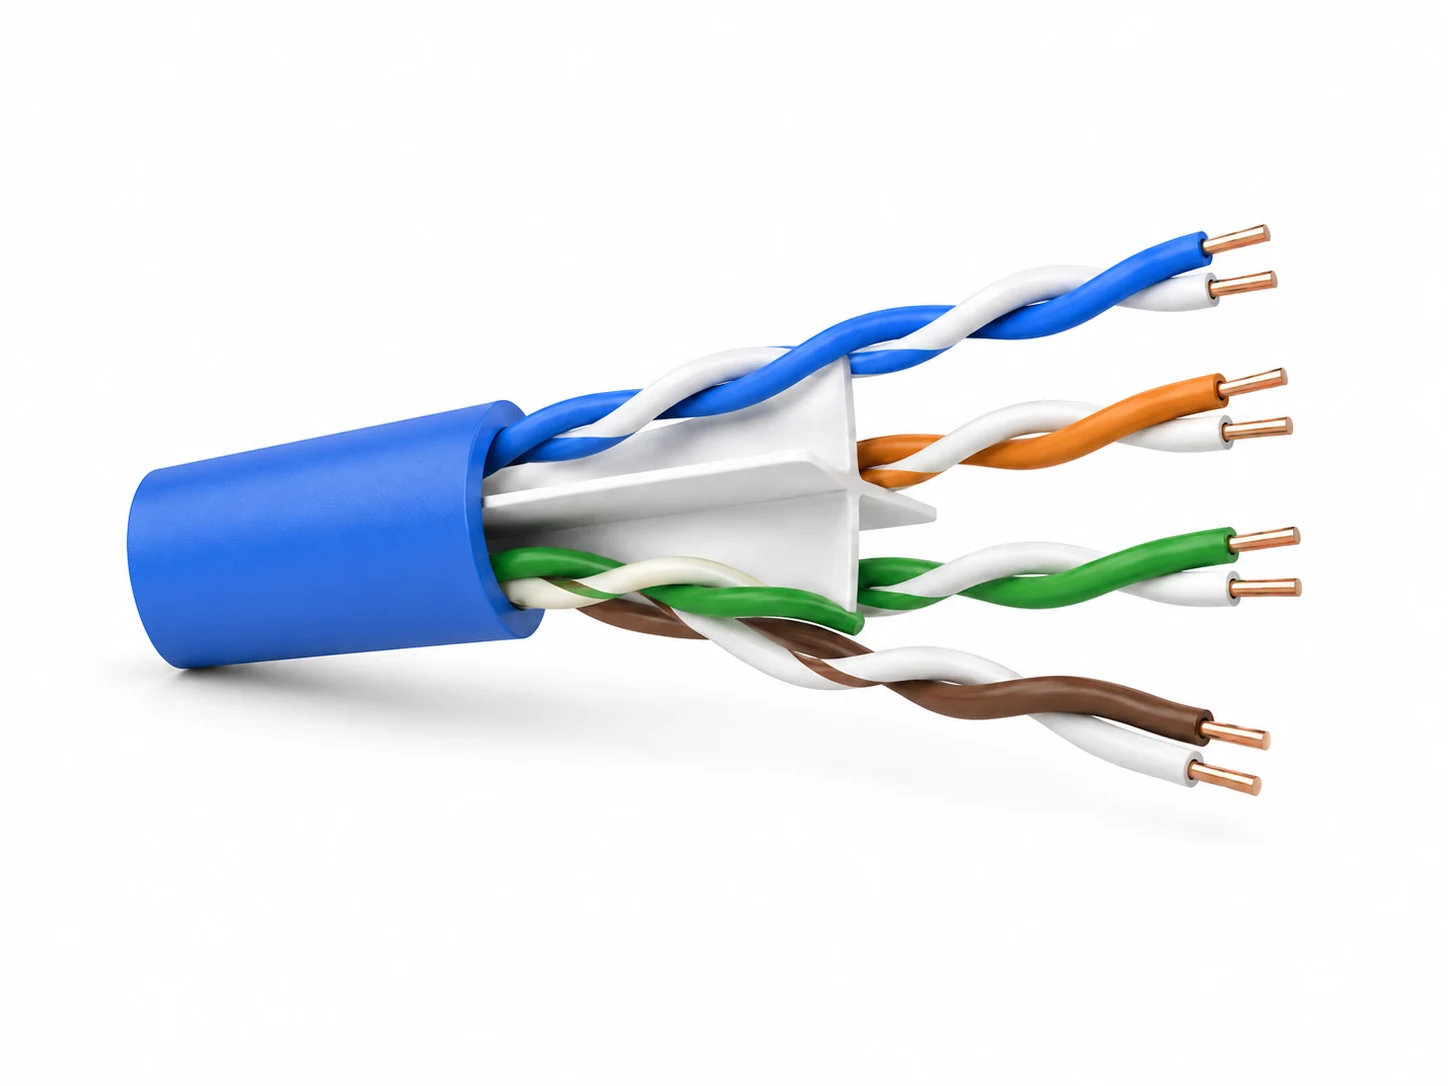
Peralatan untuk kabel twisted-pair
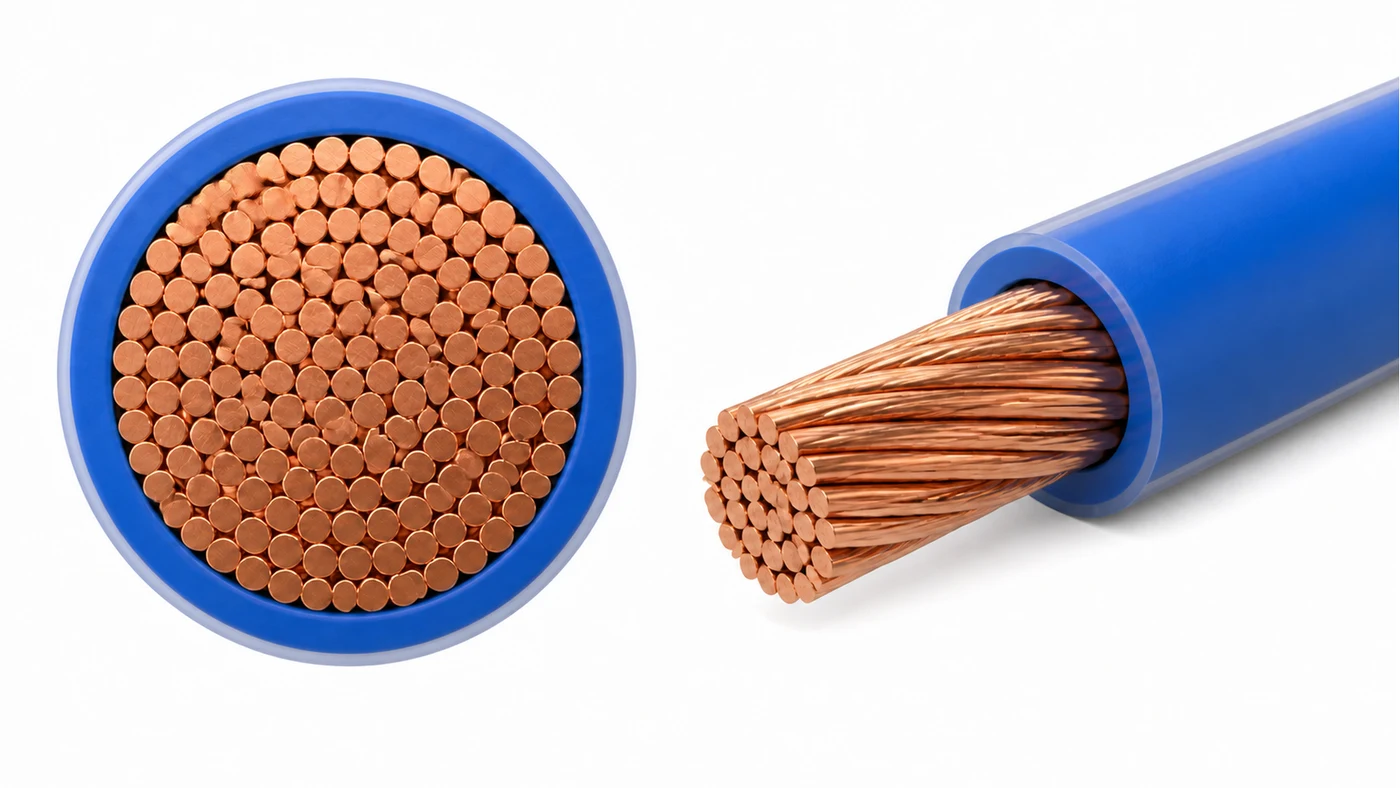
Mesin untuk kawat dan kabel berinsulasi
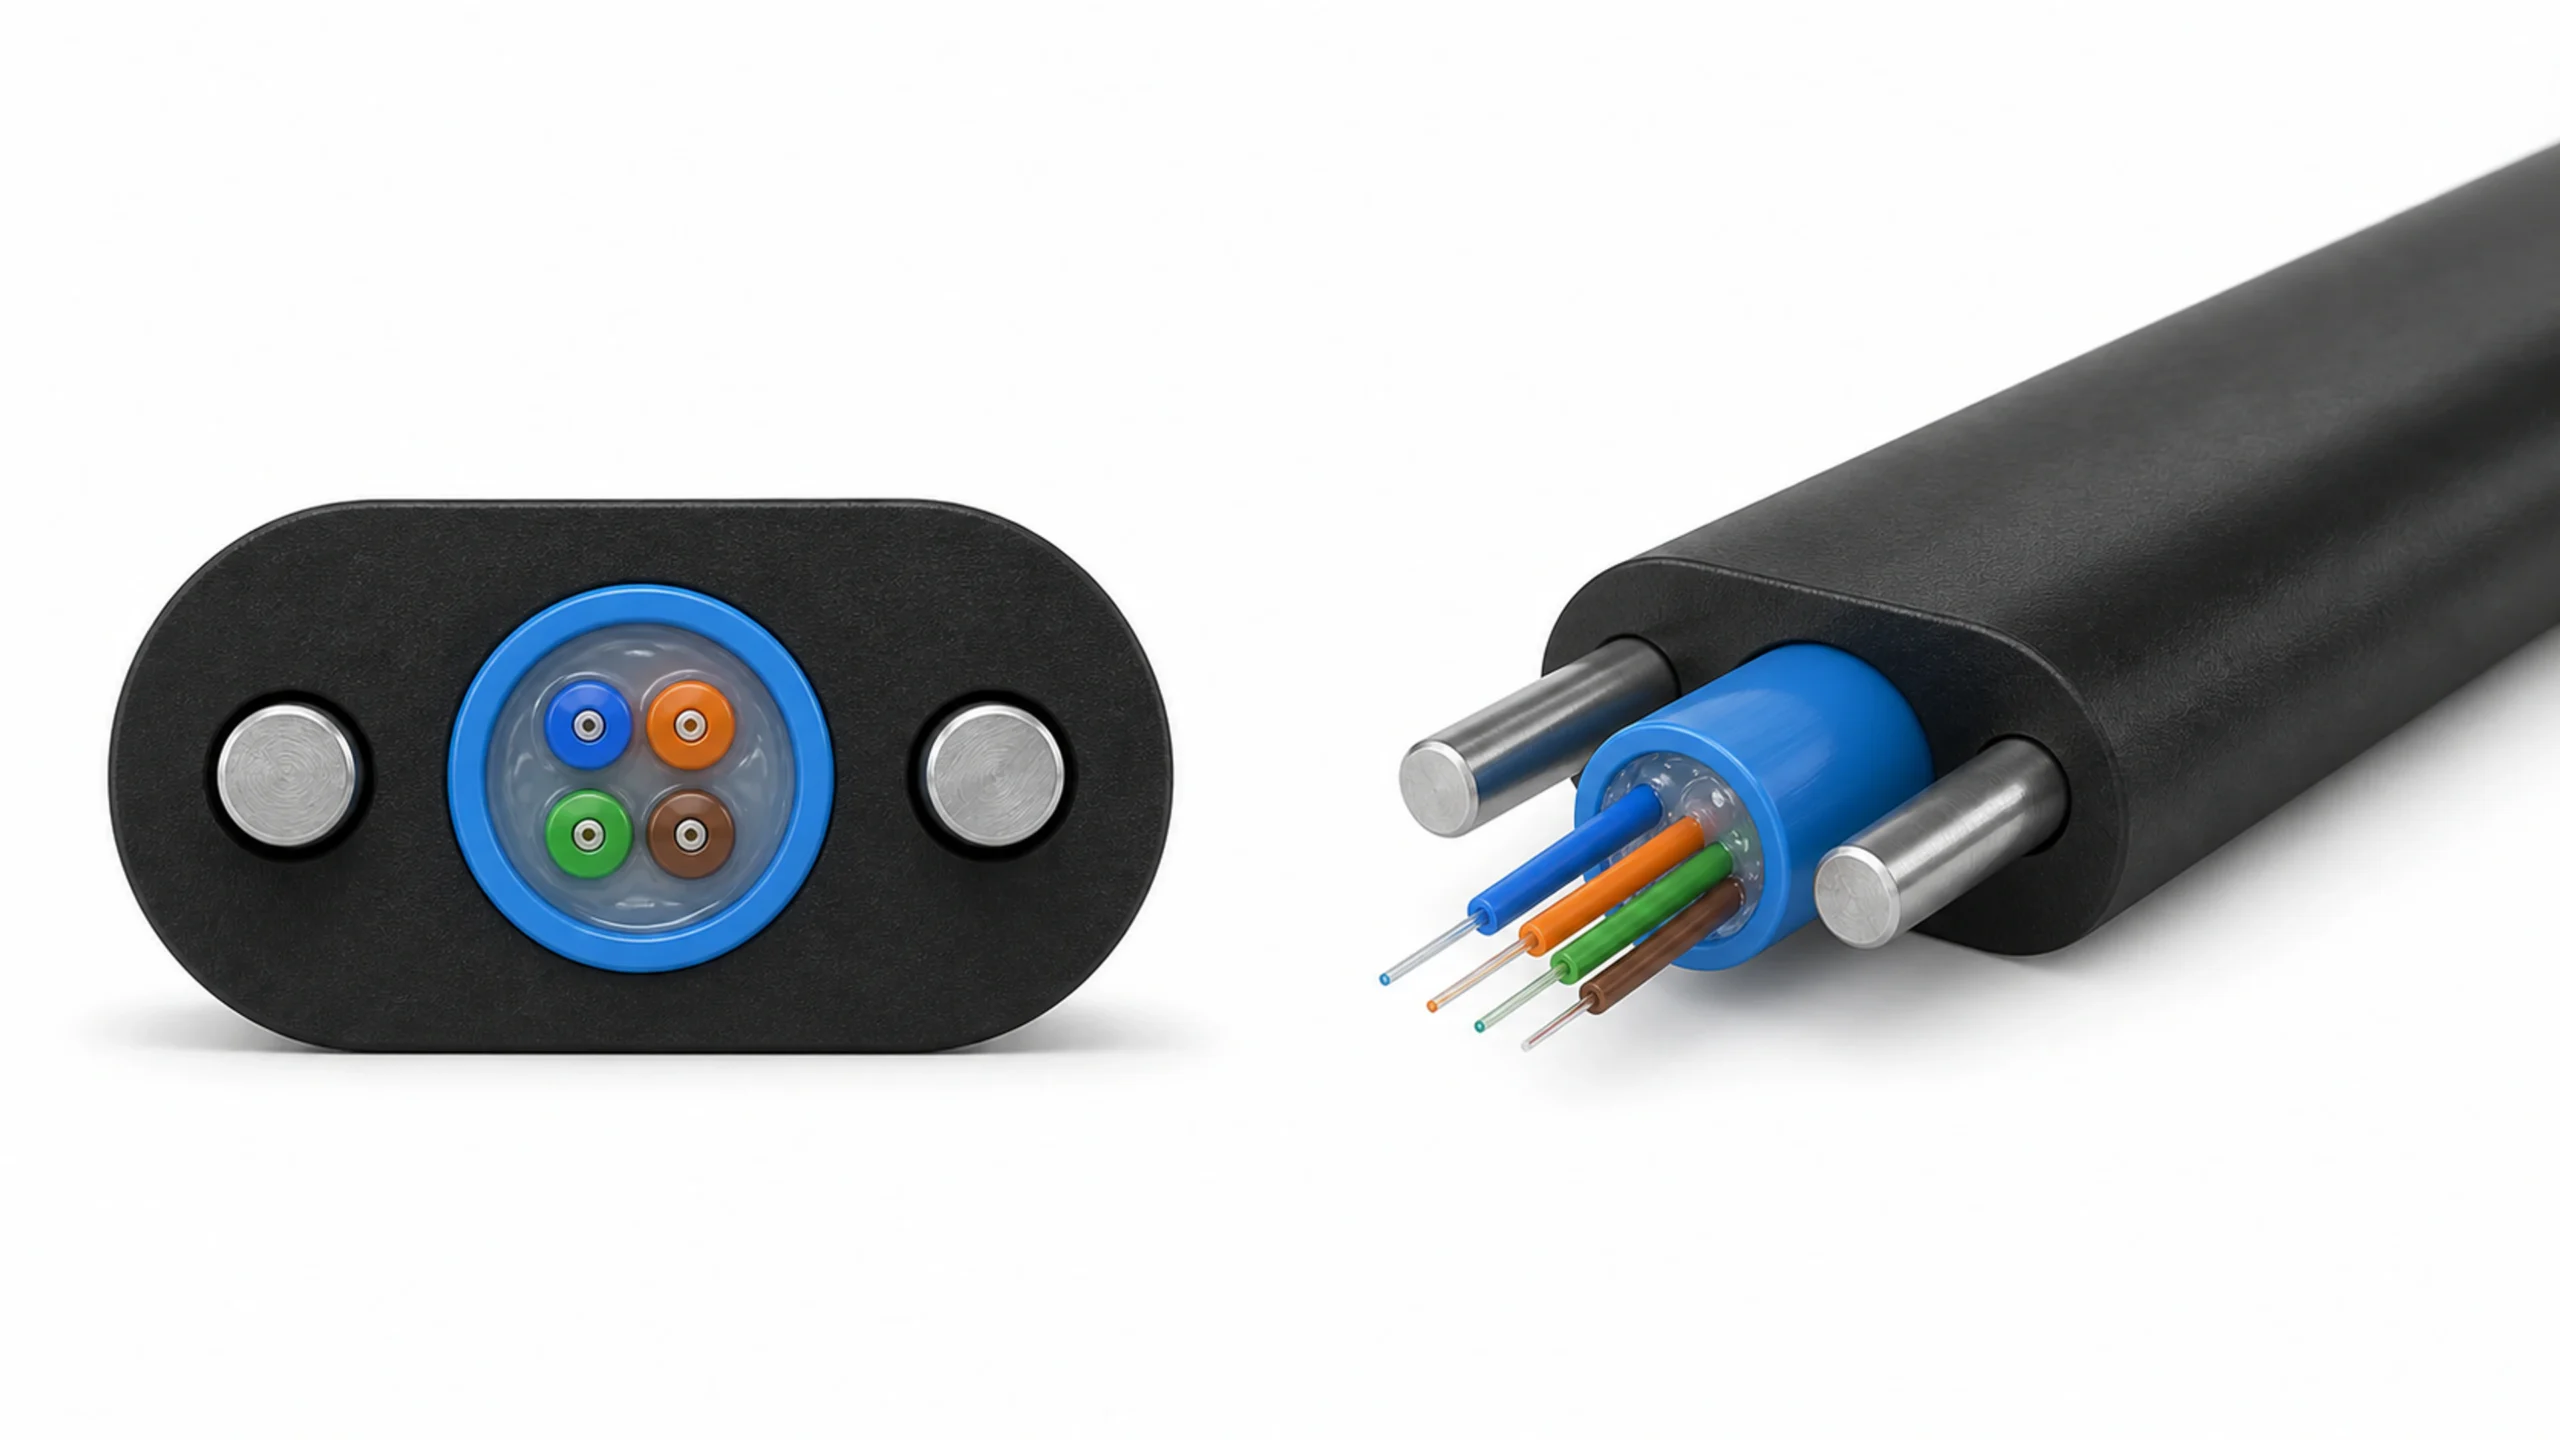
Jelajahi jenis kabel serat optik
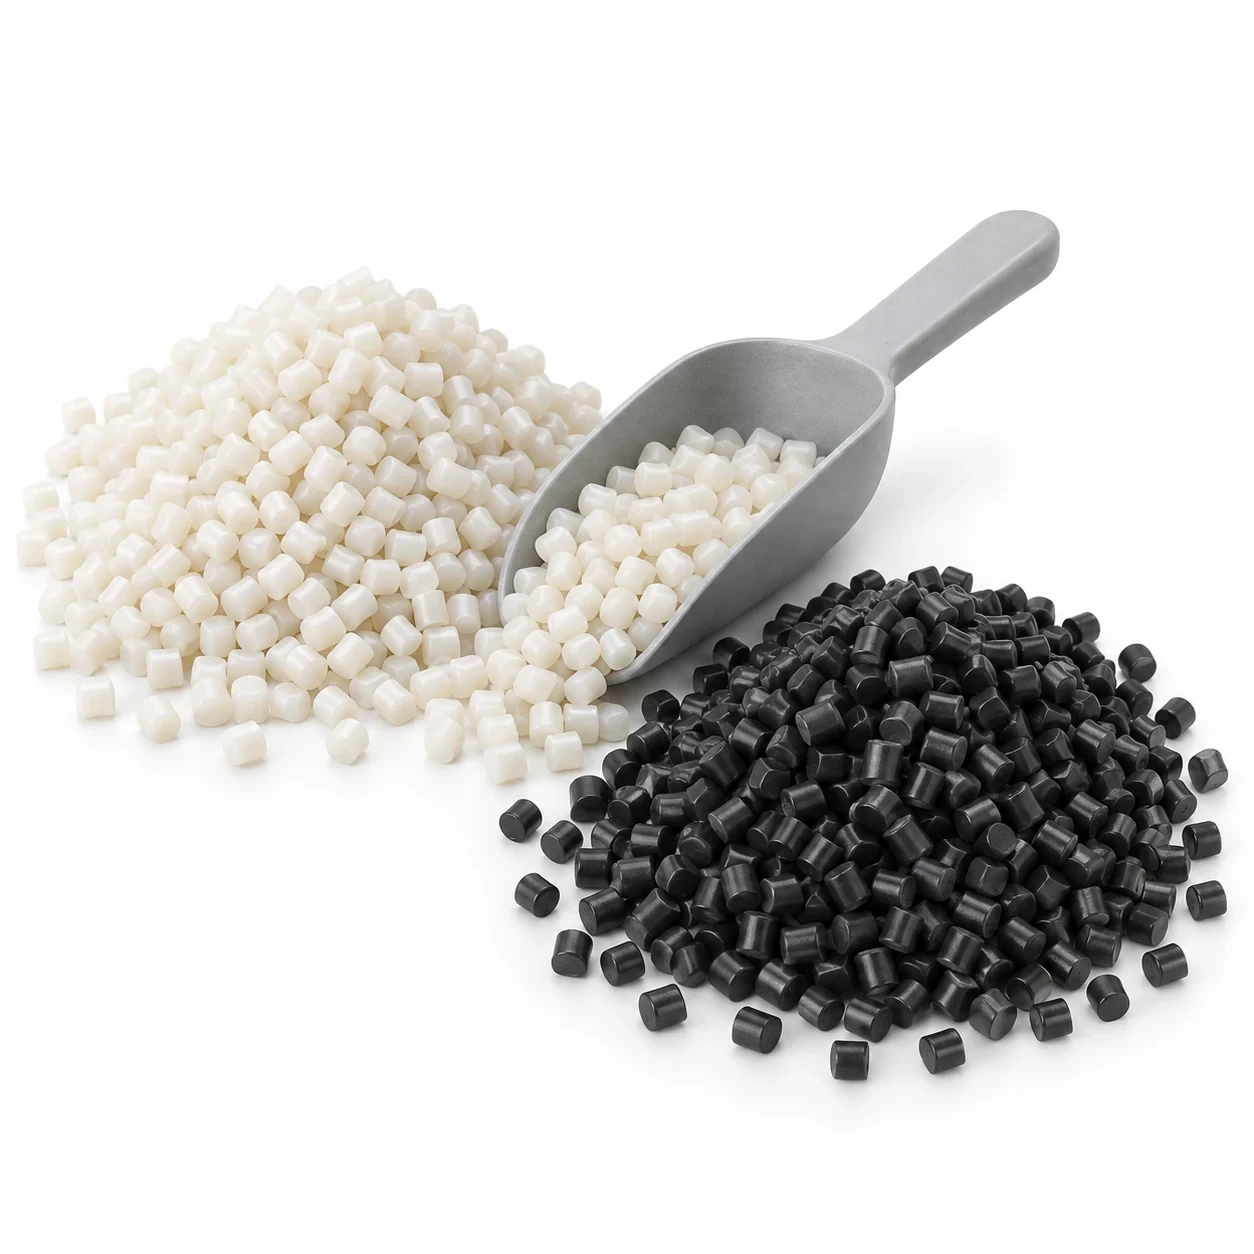
Bahan untuk produksi kabel optik
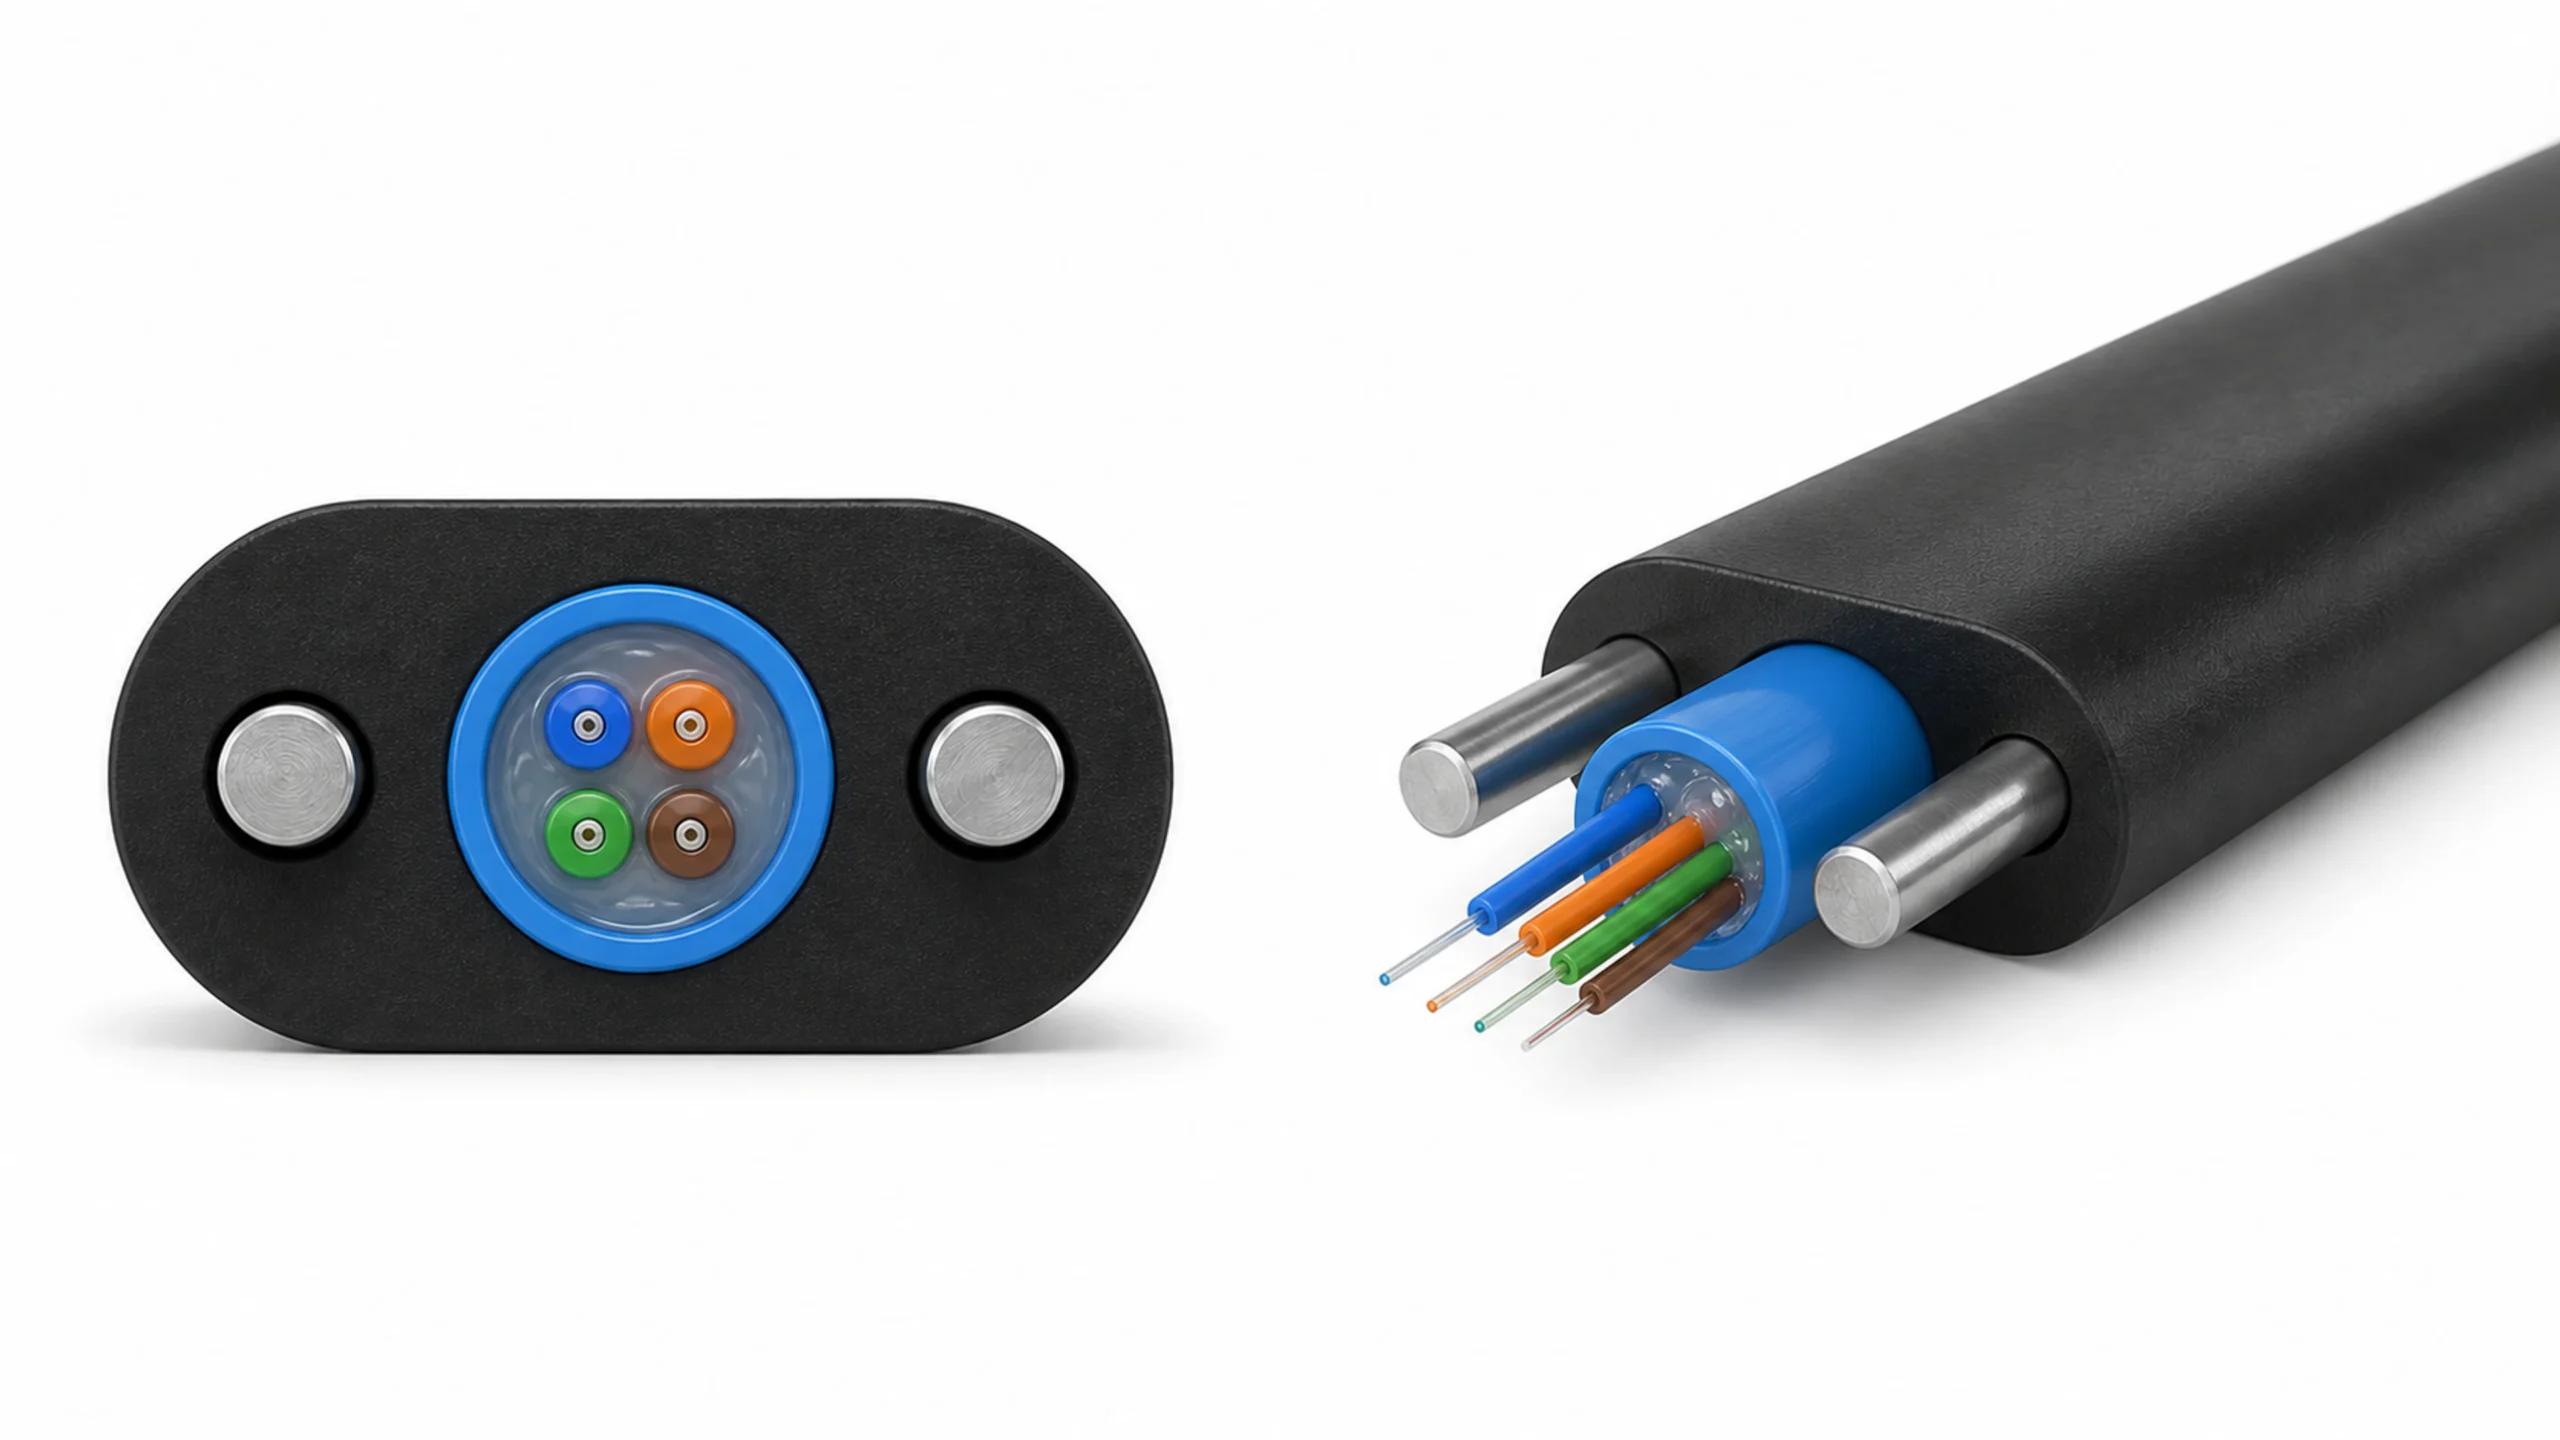
Lini kabel lengkap, material, tata letak, dan dukungan startup.

Pembuatan kabel, perakitan MPO, dan pengujian optik akhir.
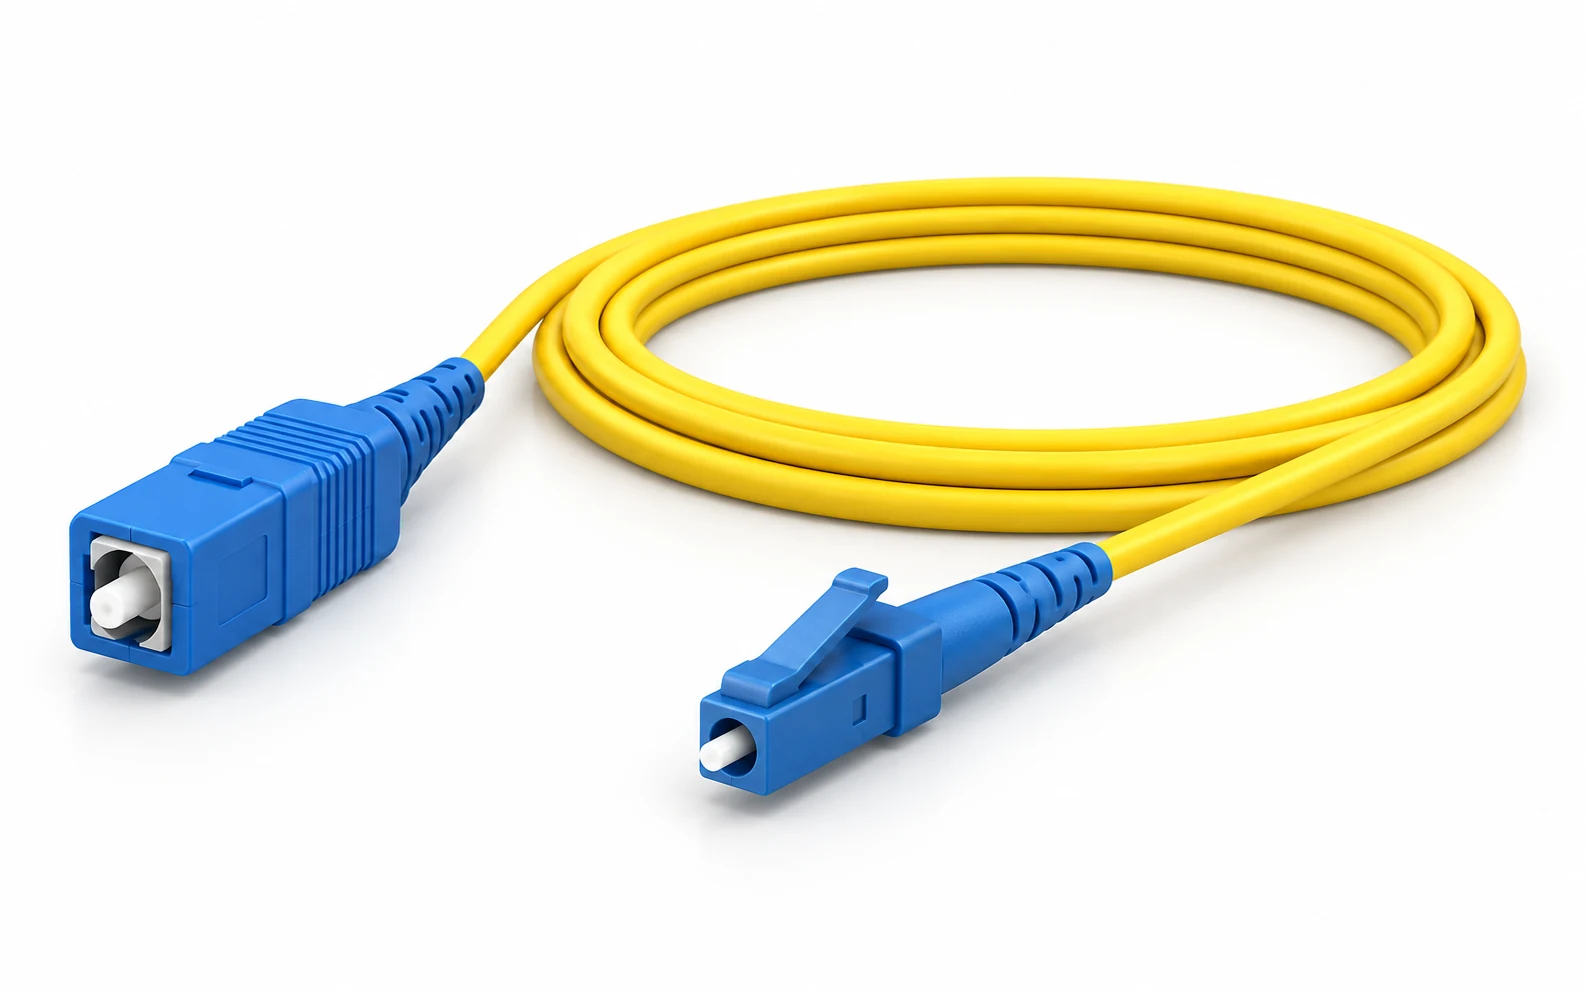
Kabel dasar, perakitan konektor, pemolesan, dan pelepasan.
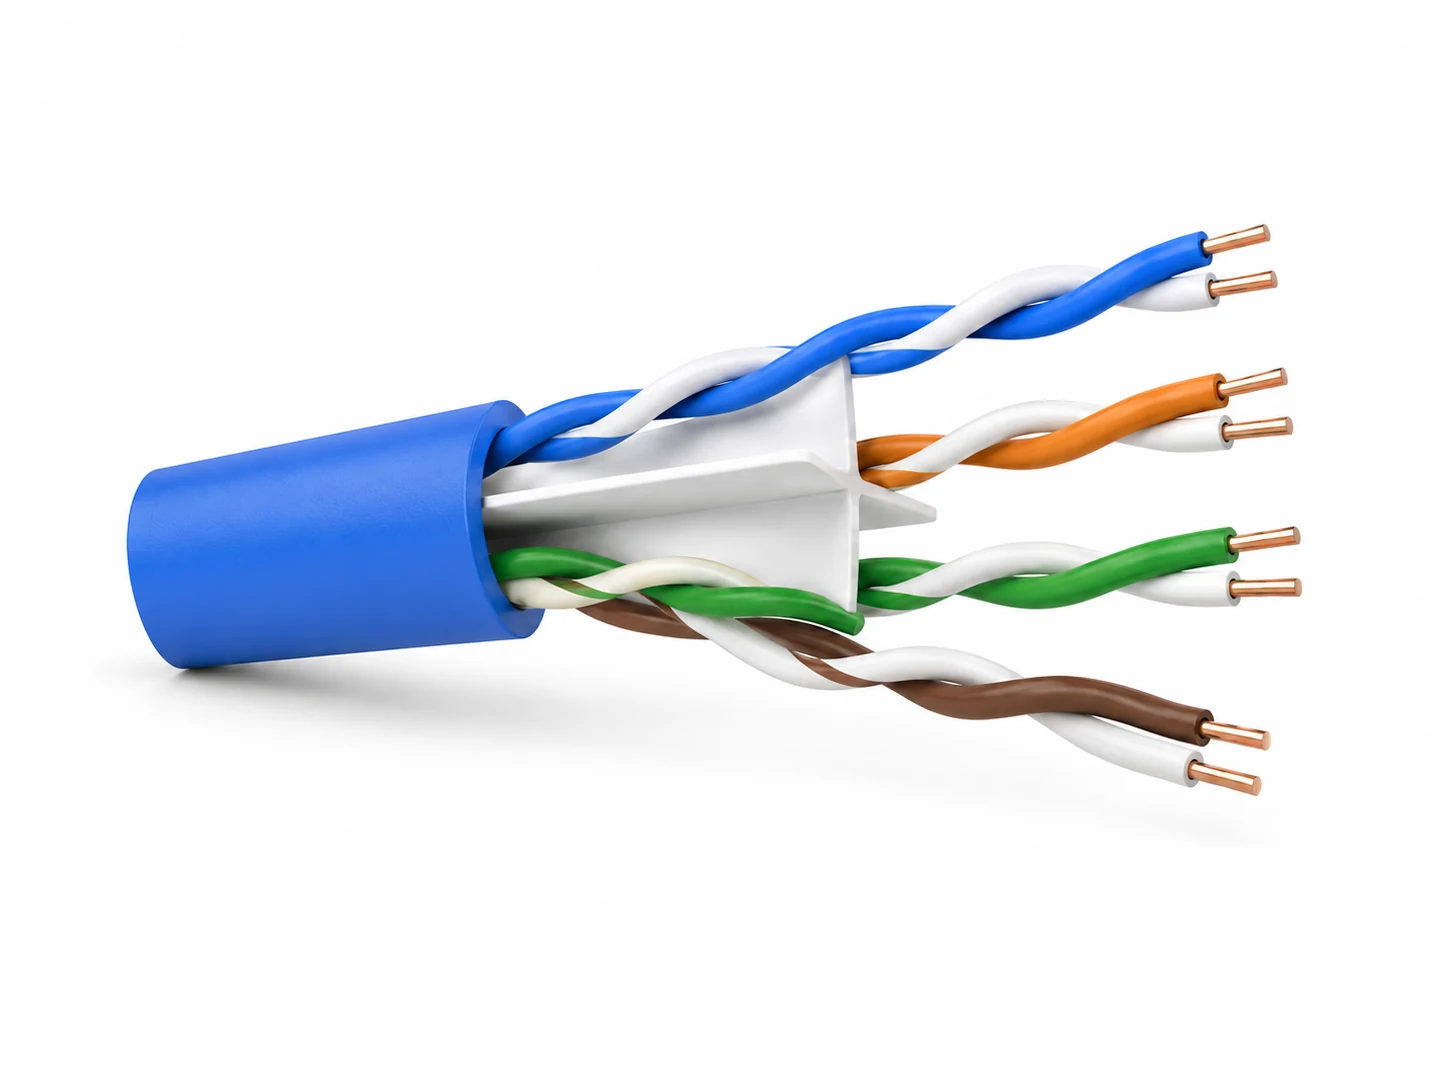
Pemilihan peralatan dan perencanaan proses untuk kabel jaringan.

01MPO CABLE & ASSEMBLY FACTORY SOLUTION
Dari serat optik hingga rakitan MPO yang telah diuji.
Solusi pabrik lengkap dengan peralatan, material, tata letak, dan keahlian untuk manufaktur kabel serta perakitan MPO presisi.
Untuk pabrik baru, produsen kabel yang sudah ada, dan bisnis perakitan yang siap berkembang.
Rencanakan Pabrik MPO SayaJelajahi seluruh proses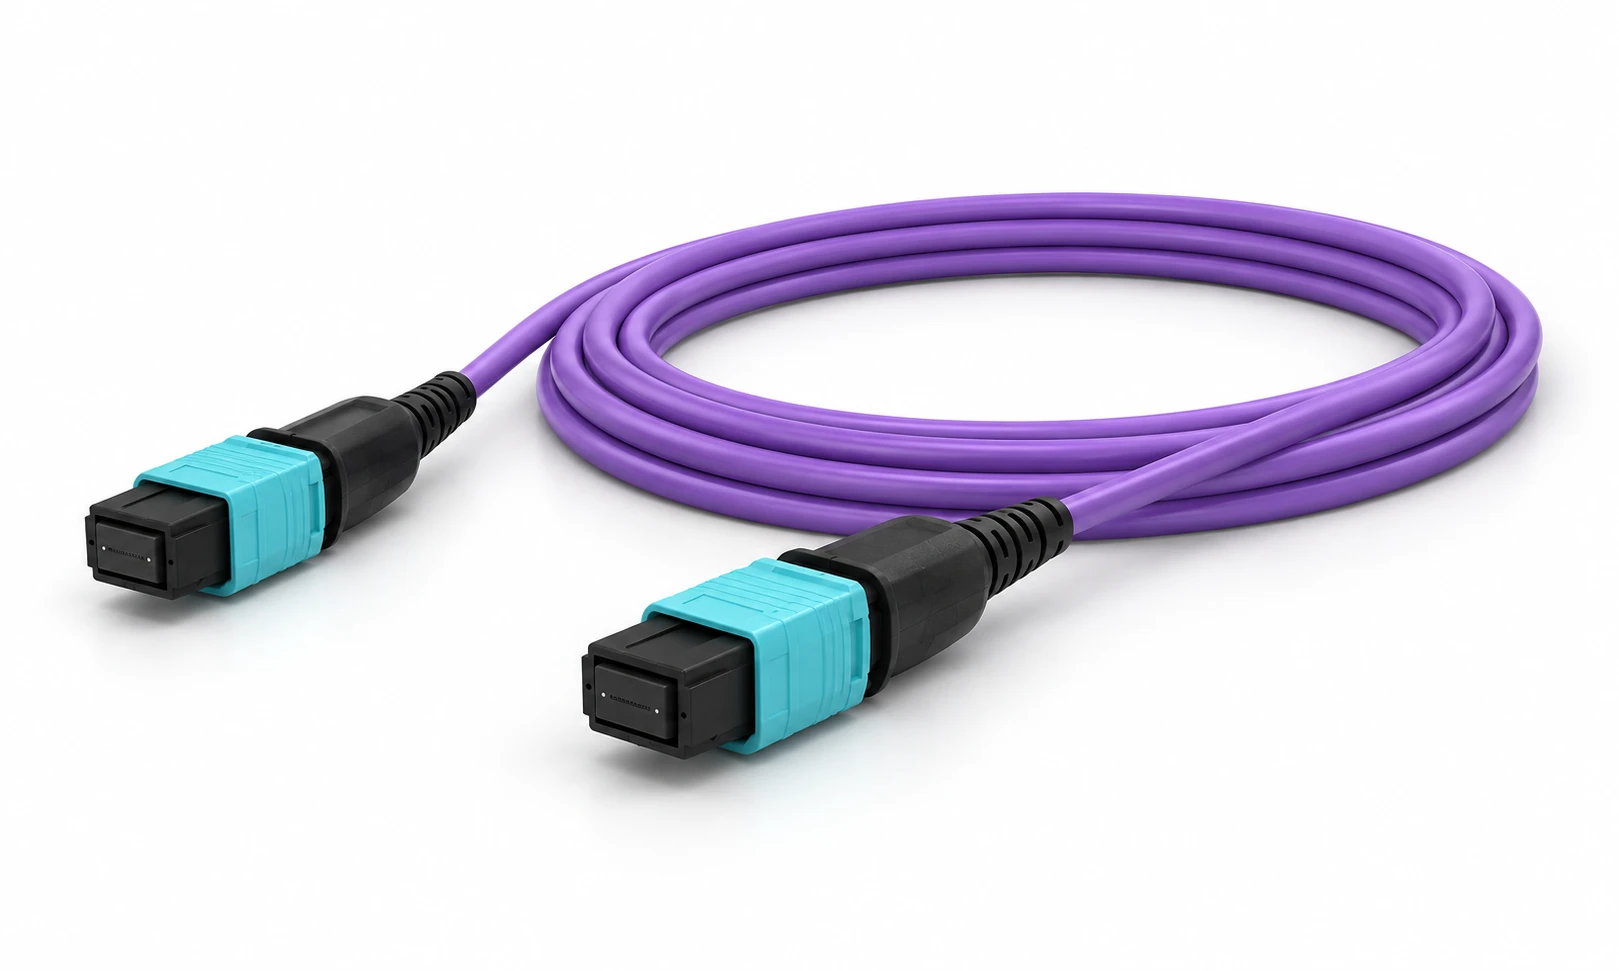
Illustrative reference.
Final scope follows the
approved product.
02INTERACTIVE PROCESS EXPLORER
See what to make, which areas are required, and how each step fits into a complete MPO factory.
STAGE 04 / 07
Individual fibers are separated, identified and arranged into a linear array for MPO termination.
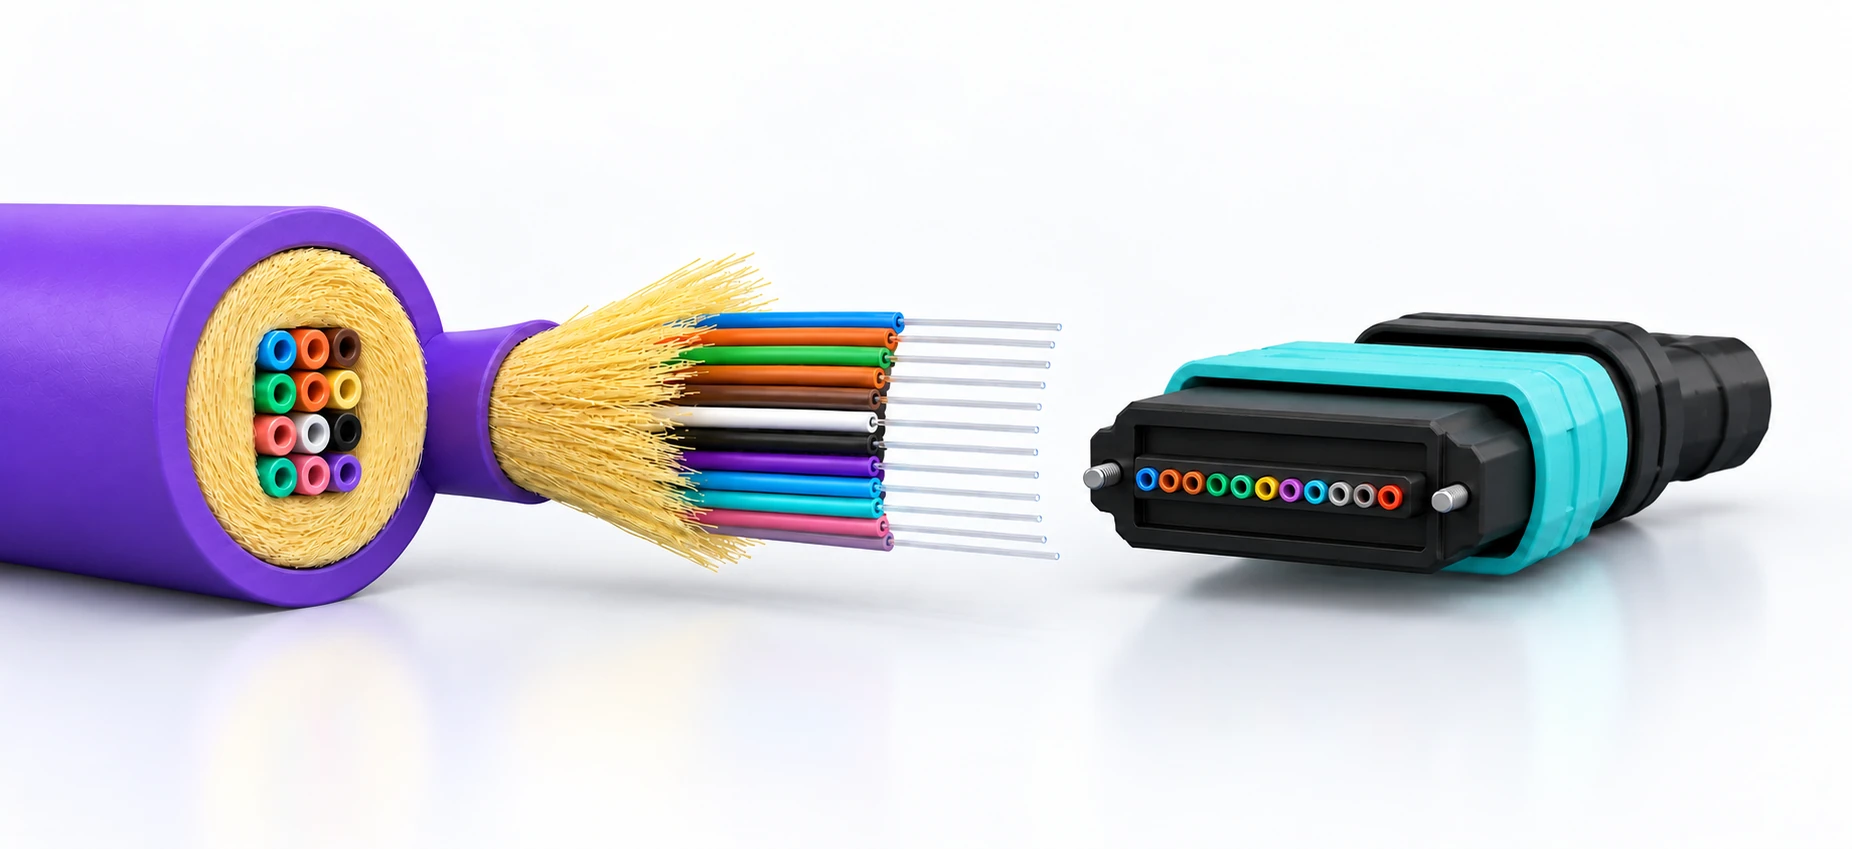
31 operations and control points across seven stages. Open a stage for its full scope.
Before production: approve the launch assembly, cable drawing, fiber category and count, connector rows, gender, key orientation, polish, channel map and acceptance plan. The signed work instruction controls the exact sequence.
Konfirmasi identitas serat, spesifikasi, kompatibilitas lapisan pelindung, nomor lot material, dan baseline optik masuk.
Pelepasan serat → persiapan terkonfigurasi → ekstrusi buffer → pendinginan → pemantauan dimensi → traksi dan penggulungan. Identifikasi setiap gulungan jadi.
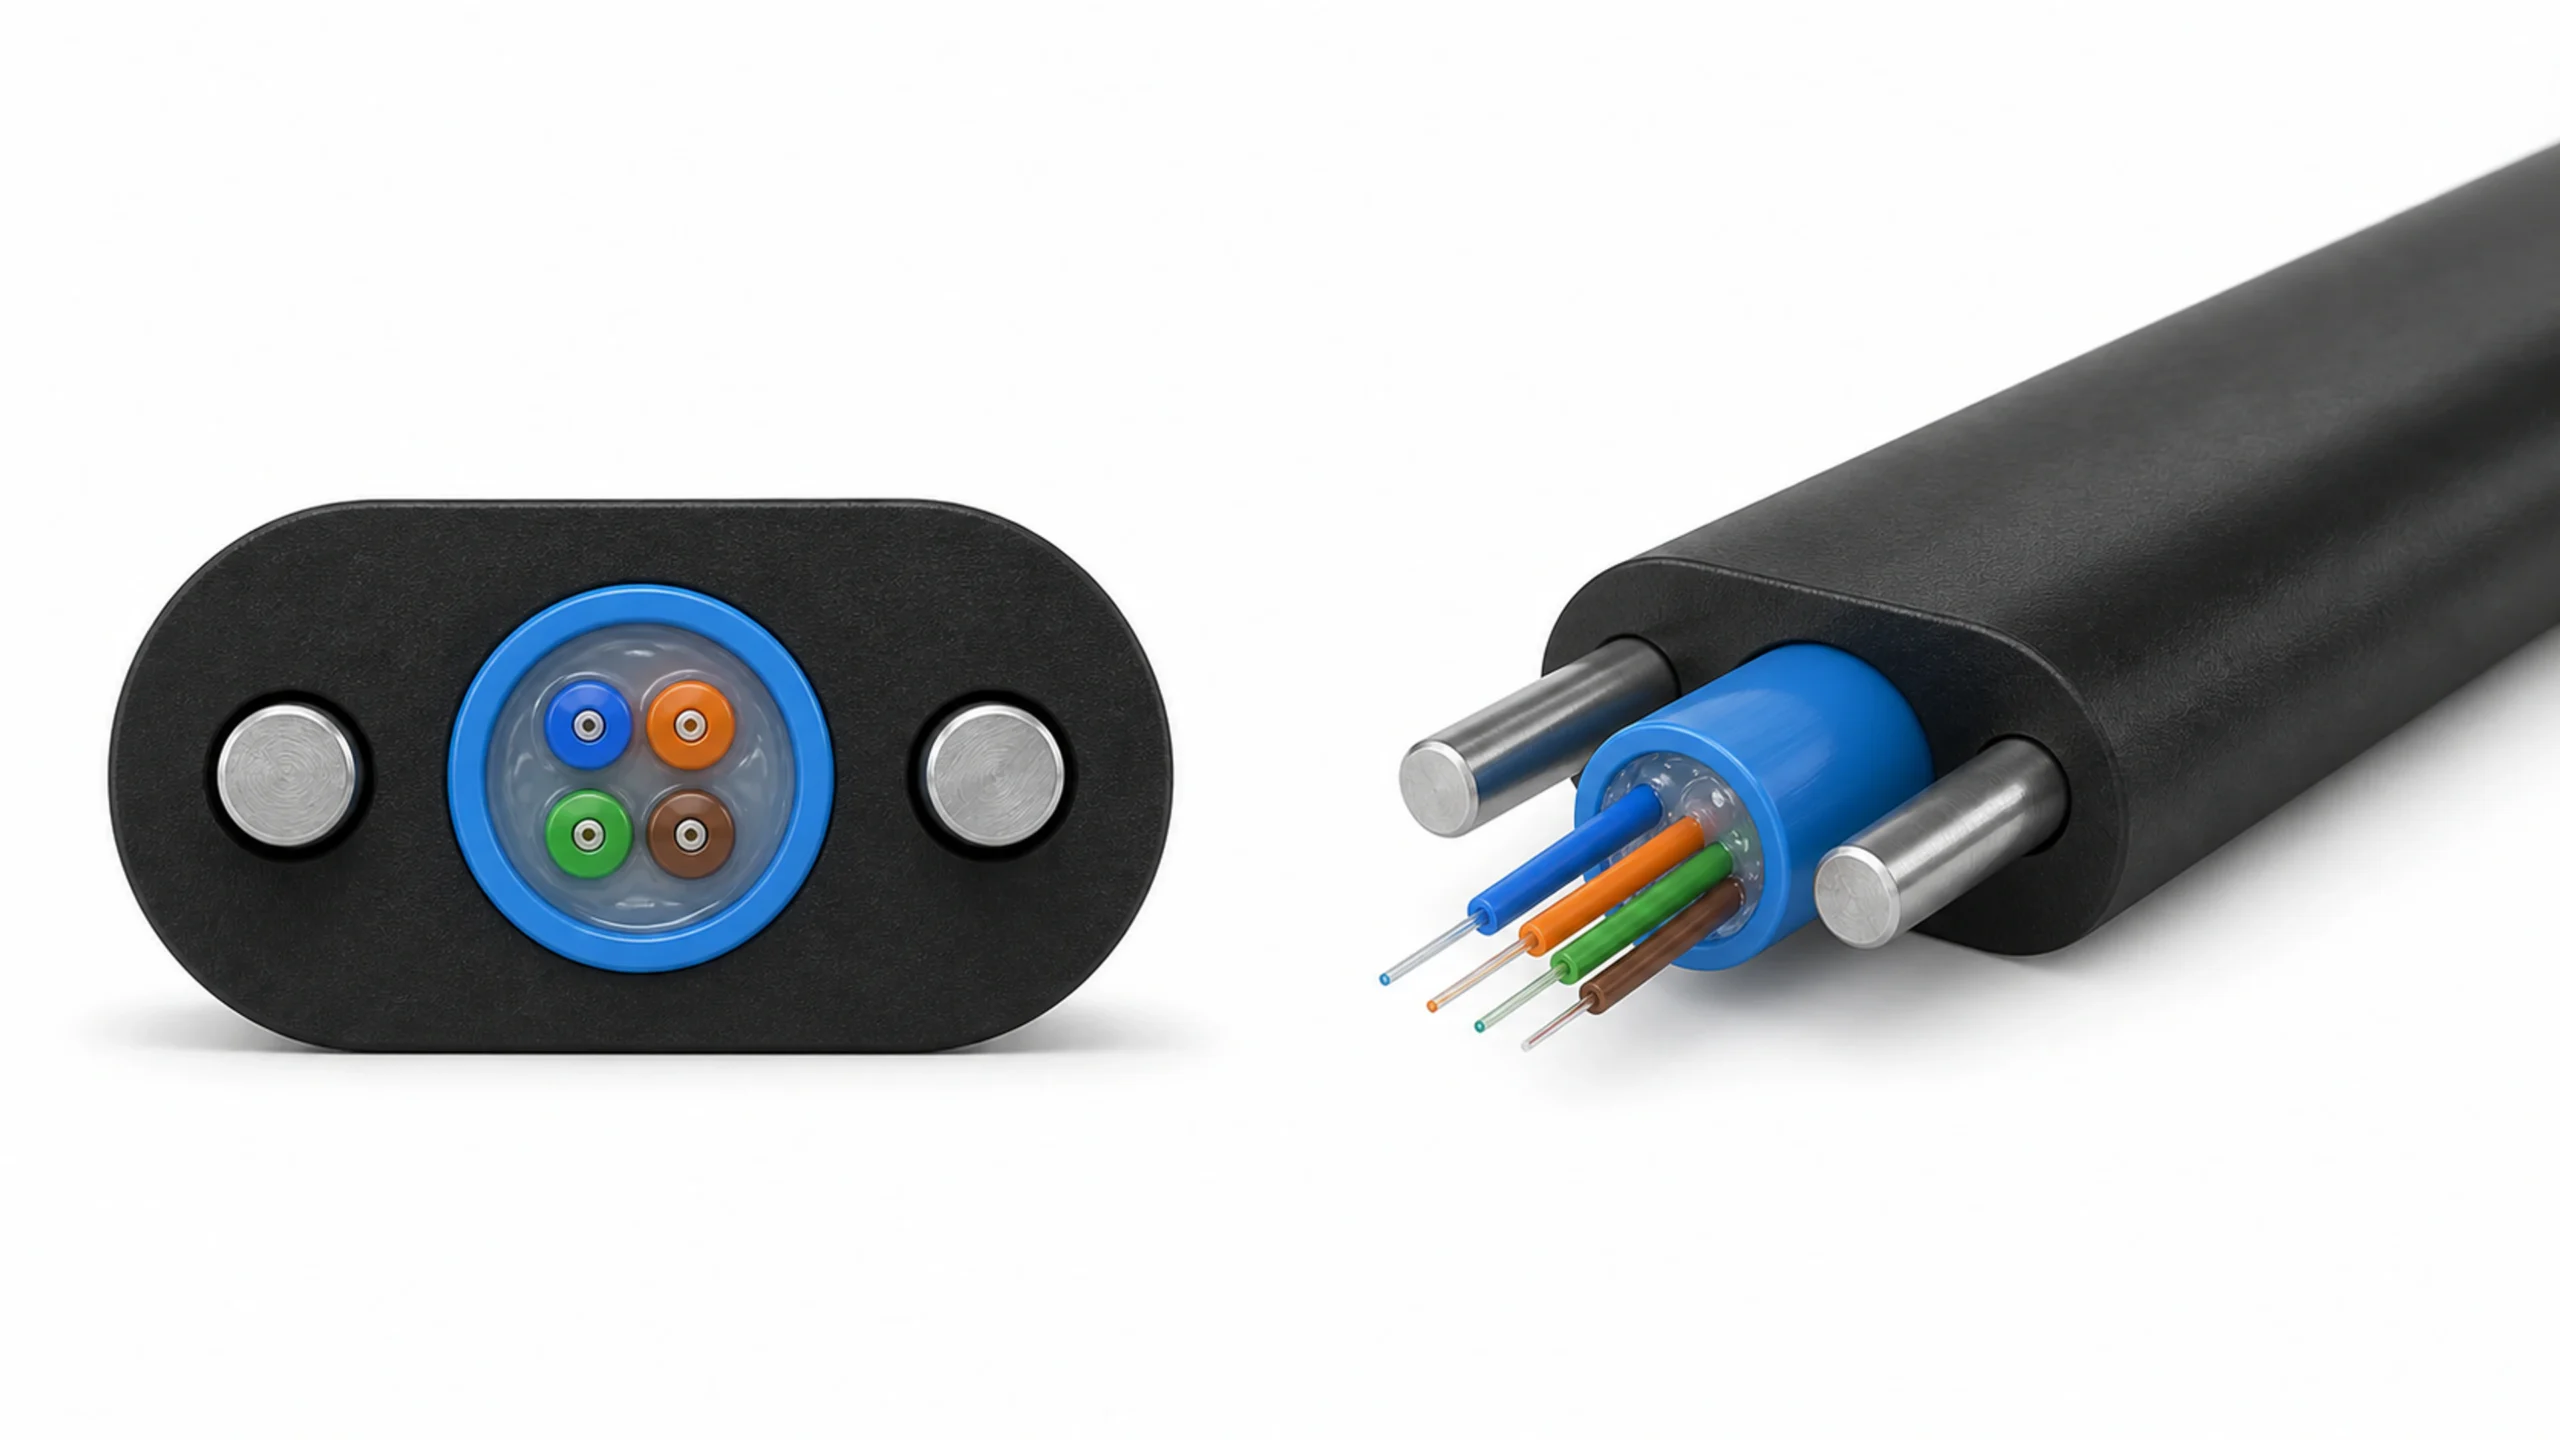
Ikuti gambar kabel dan urutan pemberian yang telah disetujui. Referensi ini membentuk inti bundel, bukan pita datar. Konfirmasi antarmuka gathering-cage.
Sesuaikan paket benang, panduan, dan tegangan terkendali dengan konstruksi yang disetujui.
Ekstrusi jaket umum → pendinginan → pemantauan diameter → capstan dan penggulung. Kaitkan gulungan jadi dengan lot serat, benang, dan polimer.
Verifikasi konstruksi, dimensi, identifikasi, kontinuitas, dan hasil optik yang disepakati terhadap rencana kontrol kabel.
Lingkup pengujian tarik, tekan, lentur, dan suhu sesuai dengan metode dan rencana pengambilan sampel yang disepakati. Instrumen laboratorium kabel terpisah dari alat ukur online dan penguji MPO.
Simpan catatan penerimaan tahap kabel. Bawa identitas gulungan sumber ke setiap panjang rakitan yang diukur dan dipotong.
Cut to the approved assembly length and branch plan. Carry source-reel identity to each piece. This operation is required even without a separately quoted cutting machine.
Ekspos panjang serat yang ditentukan dan siapkan elemen penguat tanpa merusaknya. Ikuti instruksi persiapan kabel dan konektor.
Pasang boot dan perangkat keras yang ditentukan pada kabel sesuai urutan yang ditetapkan konektor sebelum operasi selanjutnya menghalangi akses. Verifikasi set komponen terhadap BOM perakitan.
Use thermal stripping only with a compatible fiber/coating and approved instruction. Check stripped length and fiber damage.
Identify and place each fiber in its approved linear position. The arranger does not choose or create polarity.
Use a holder matched to fiber count, pitch and material. Recheck order after clamping and retain an identified array record.
Check the selected ferrule, adhesive, process liquids, shelf life, preparation and working time. The work instruction determines the adhesive-and-fiber loading sequence.
Use centrifugal degassing only when required by the material instruction. Link the batch, usable-life status and preparation cycle to the ferrules.
Unit hisap yang dikutip bukanlah metode pengisian universal. Konfirmasikan penggunaan, pengaturan, dan verifikasinya sesuai dengan instruksi konektor dan material.
Confirm ferrule lot, orientation and loaded-array order. This is a required operation; the reference equipment list does not establish a separate powered loader.
Gunakan resep perekat yang memenuhi syarat. Catat pemegang, batch, muatan, bukti waktu-suhu, dan inspeksi pasca-pengawetan. Jumlah oven saja tidak membuktikan kapasitas.
Perform at the connector-defined point, which may differ from this overview order. Prove matched jaws and tooling with the actual housing and aramid arrangement.
Use the connector-approved preparation method and revision. Check the identified ferrule before it enters the polishing route.
Tentukan batas pelepasan dan apakah pengerokan merupakan bagian dari produksi normal atau diperbolehkan sebagai pengerjaan ulang. Simpan bukti sebelum/sesudah serta pemeriksaan kerusakan.
Match ferrule and polish geometry. The referenced 24-position fixture counts holding positions, not fibers or guaranteed output.
Control load, time, films, pads, cloths, liquids and the cleaning sequence. Retain recipe revision, consumable lots and permitted rework history.
Sertakan hanya setelah mengonfirmasi objek yang diproses, cairan, waktu, dan kompatibilitasnya. Ini bukan langkah pembersihan otomatis untuk setiap perakitan MPO.
Gunakan metode pembersihan yang telah disetujui dan kontrol penanganan. Lindungi permukaan akhir dan serahkan rakitan yang telah diidentifikasi untuk diperiksa.
Use a qualified MPO adapter. Retain identified full-array images and the clean → re-inspect → disposition record. Visual inspection does not replace geometry or optical tests.
Apply the agreed attributes, limits and inspection plan. Retain raw reports, adapter/reference identity and repeatability evidence.
Periksa kedua ujung terhadap peta saluran yang telah ditandatangani, jenis kelamin, dan orientasi kuncinya. Alat uji mendeteksi kesalahan pemetaan; alat ini tidak memperbaikinya.
Match wavelengths, metrics, directions, references and limits to the product. The quoted system is a multimode reference; single-mode and return-loss needs require separate scope review.
Hubungkan rakitan akhir ke gulungan sumbernya, lot komponen, dan hasil tingkat saluran. Pasang tutup pelindung dan simpan catatan pelepasan serta pengemasan.
Shell removal is rework only unless the connector instruction explicitly states otherwise. Confirm housing compatibility and use limits. After permitted reassembly or rework, repeat the required inspection, polarity and optical checks. Retain the original failed result as well as the repeat results.
03COMPLETE FACTORY FLOW
Area manufaktur dan perakitan terpisah.
Titik rilis yang jelas. Catatan produksi terhubung.
Manufacture and release the MPO base cable.
Complete, test and release finished MPO assemblies.
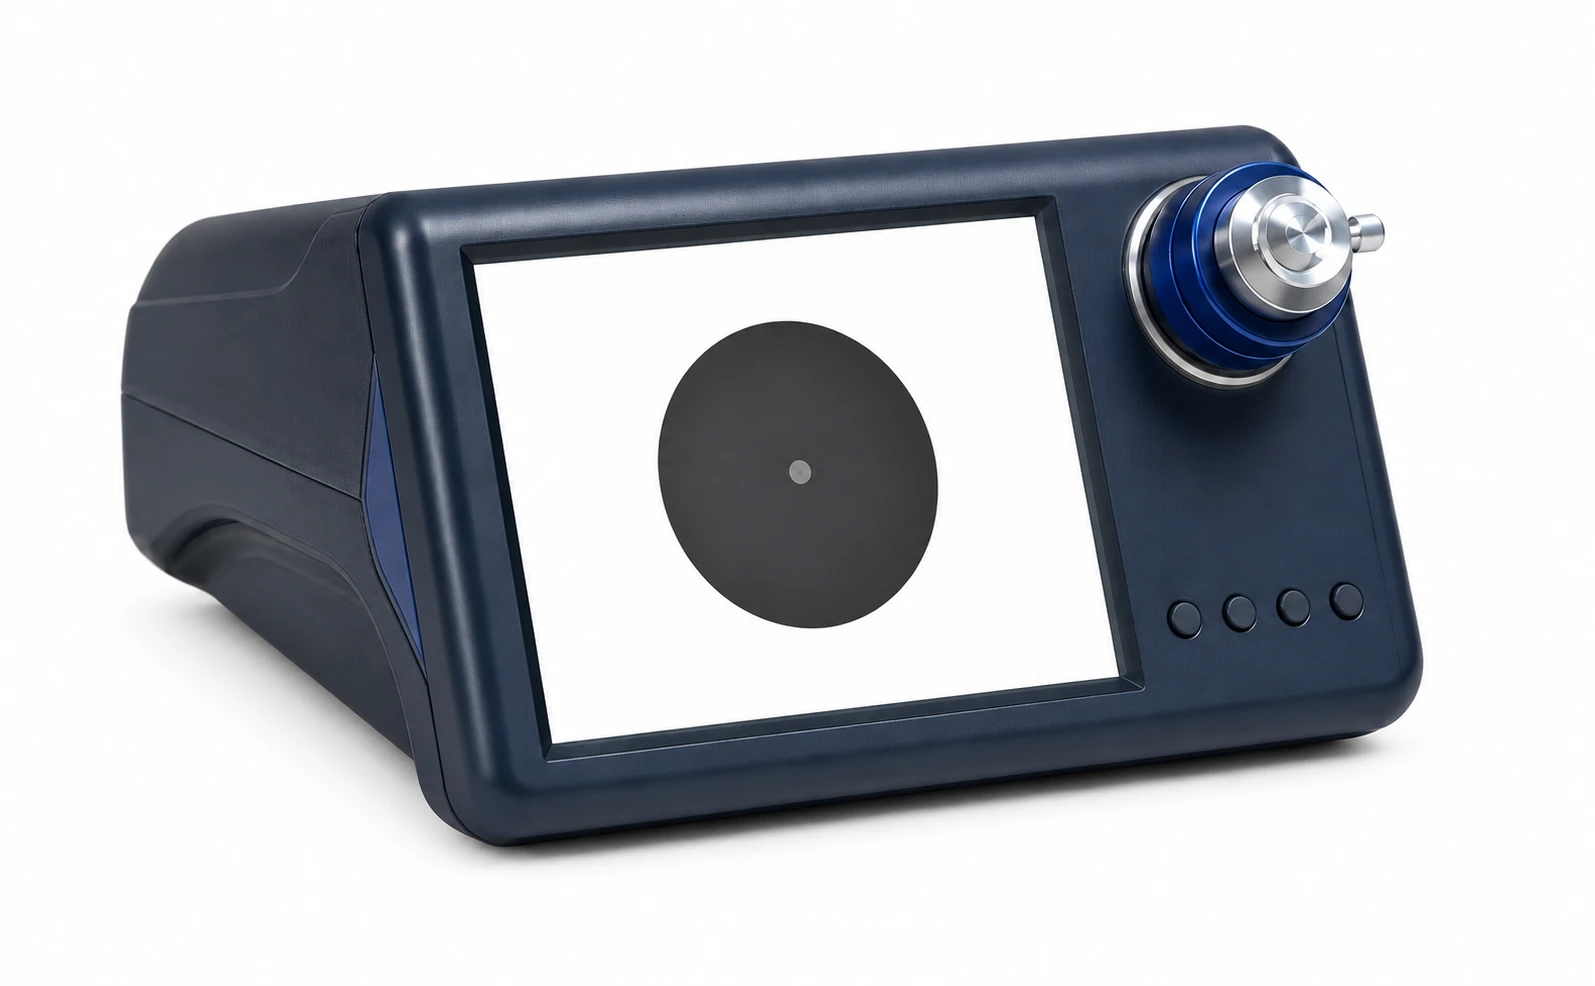
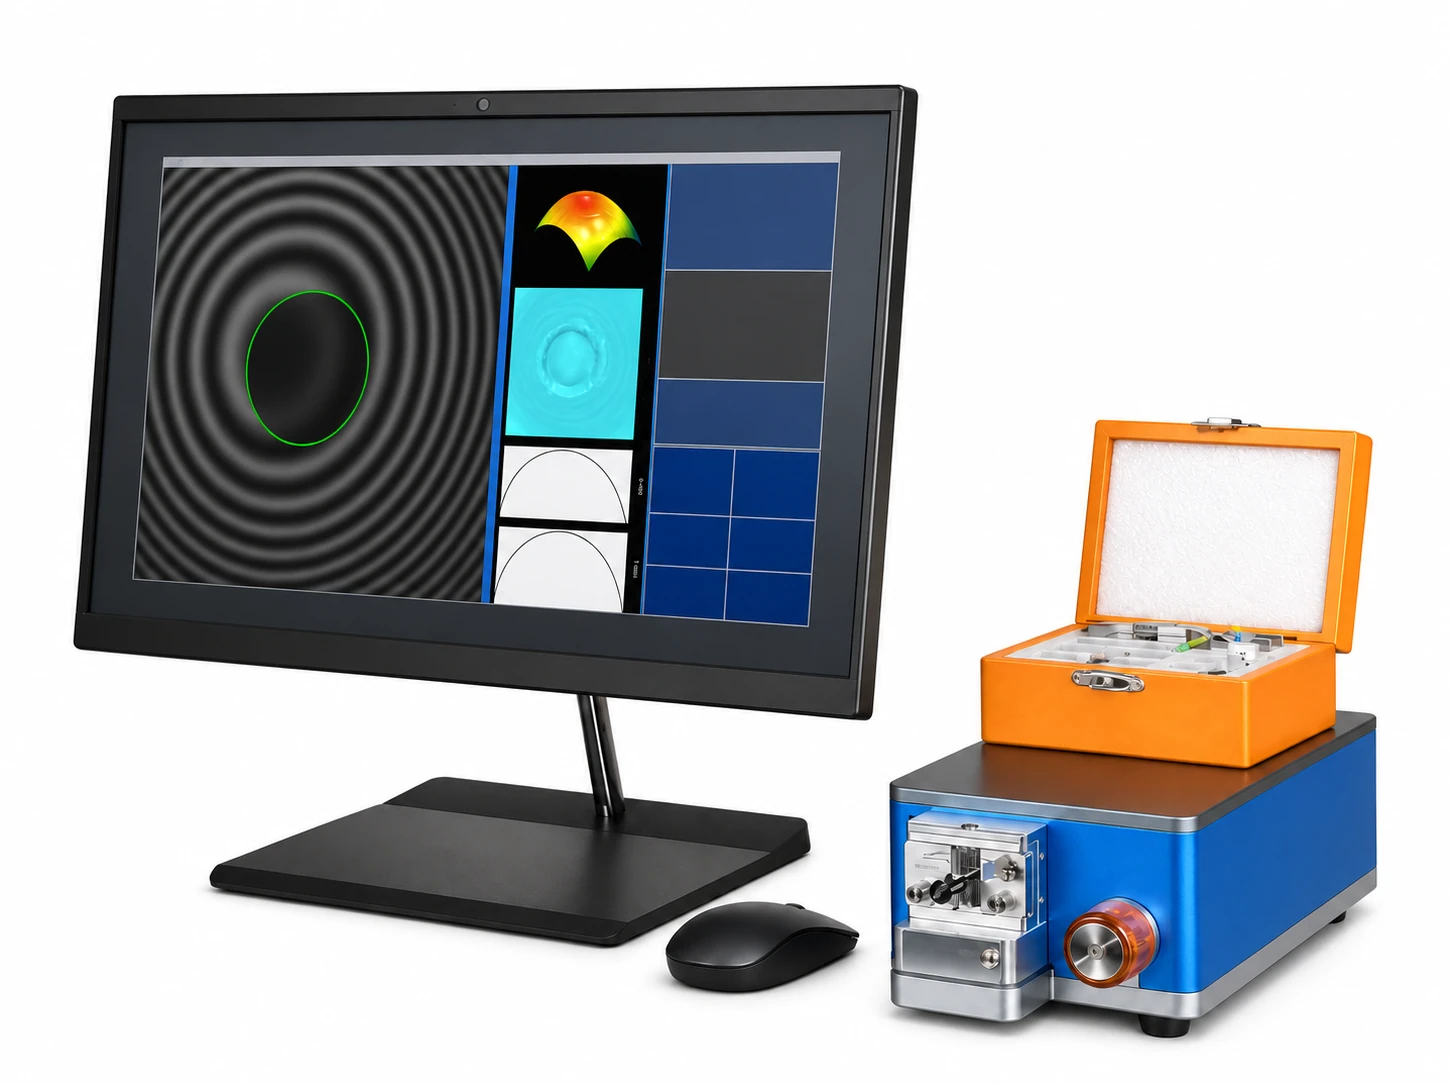
Satu identitas rakitan. Keep the link from input fiber reel to finished cable reel, cut length, component lots, ferrule, cure and polishing recipe, inspection images and channel results.
Simpan catatan yang gagal dan dikerjakan ulang. Kelulusan optik tidak menggantikan bukti penerimaan kabel dasar tersebut.
04PROJECT REQUIREMENT SNAPSHOT
The first decision is your launch assembly. It defines the cable construction, connector workcells and evidence needed for release.
Buat ringkasan proyek AndaThe illustrated launch example is a 12-fiber GJFJV-type cable feeding MPO assembly. Other constructions require a matched route.
05EQUIPMENT BY PRODUCTION STAGE
Complete cable lines, specialist assembly tools and separate release instruments.
A complete line for individually buffered fibers: payoff, extrusion, cooling, dimensional control and take-up. Confirm the fiber, buffer material, tooling and release method.
An HK-50 reference configuration with matched fiber gathering, aramid handling, common-jacket extrusion, cooling and take-up. State whether the gathering cage is integrated or separately matched.
Equipment names open a production-line page or the matching equipment process guide. Select an image for scope and acceptance notes. “Launch route” refers to this reference product, not every MPO design. Equipment illustrations show a reference configuration. Confirm the final equipment scope for your project.
06RAW MATERIALS & INITIAL BOM SUPPORT
Plan the cable inputs, connector components and process consumables together, so the first production run has a complete material path.
Sesuaikan tingkat material dengan gambar kabel dan jendela proses sebelum menentukan ukuran batch produksi pertama.
Jelajahi bahan kabel
Kategori serat, kompatibilitas lapisan, identitas gulungan, dan pemeriksaan masuk.
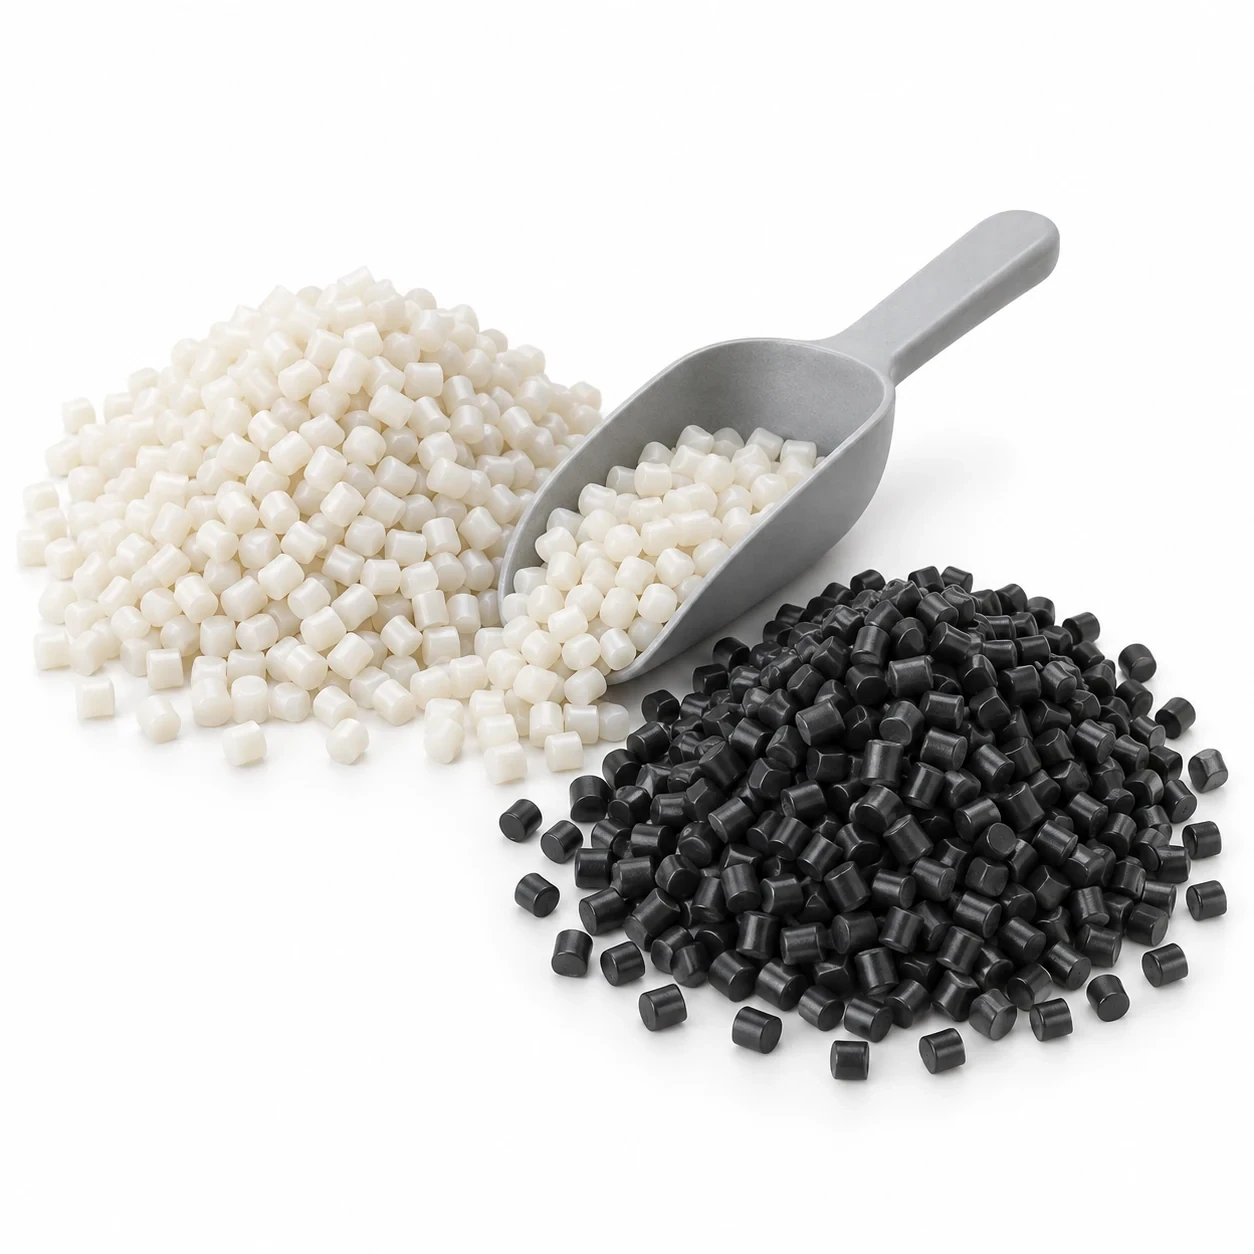
Separate tight-buffer and outer-jacket grades; agree processing and storage conditions.

Konstruksi, kerapatan linear, rentang tegangan, dan kompatibilitas kemasan.
Referensi material ilustratif. Komponen, mutu, dan bahan habis pakai yang tepat mengikuti produk dan proses yang telah disetujui.
Material specifications, supplier review, sample checks and an initial cable BOM.
07FACTORY LAYOUT & UTILITIES
Hubungkan alur material. Pisahkan pekerjaan pembuatan kabel berat dari perakitan konektor presisi.
Rencanakan panjang mesin, akses layanan, rute gulungan, pengangkatan, dan lorong aman di sekitar peralatan yang telah dikonfirmasi.

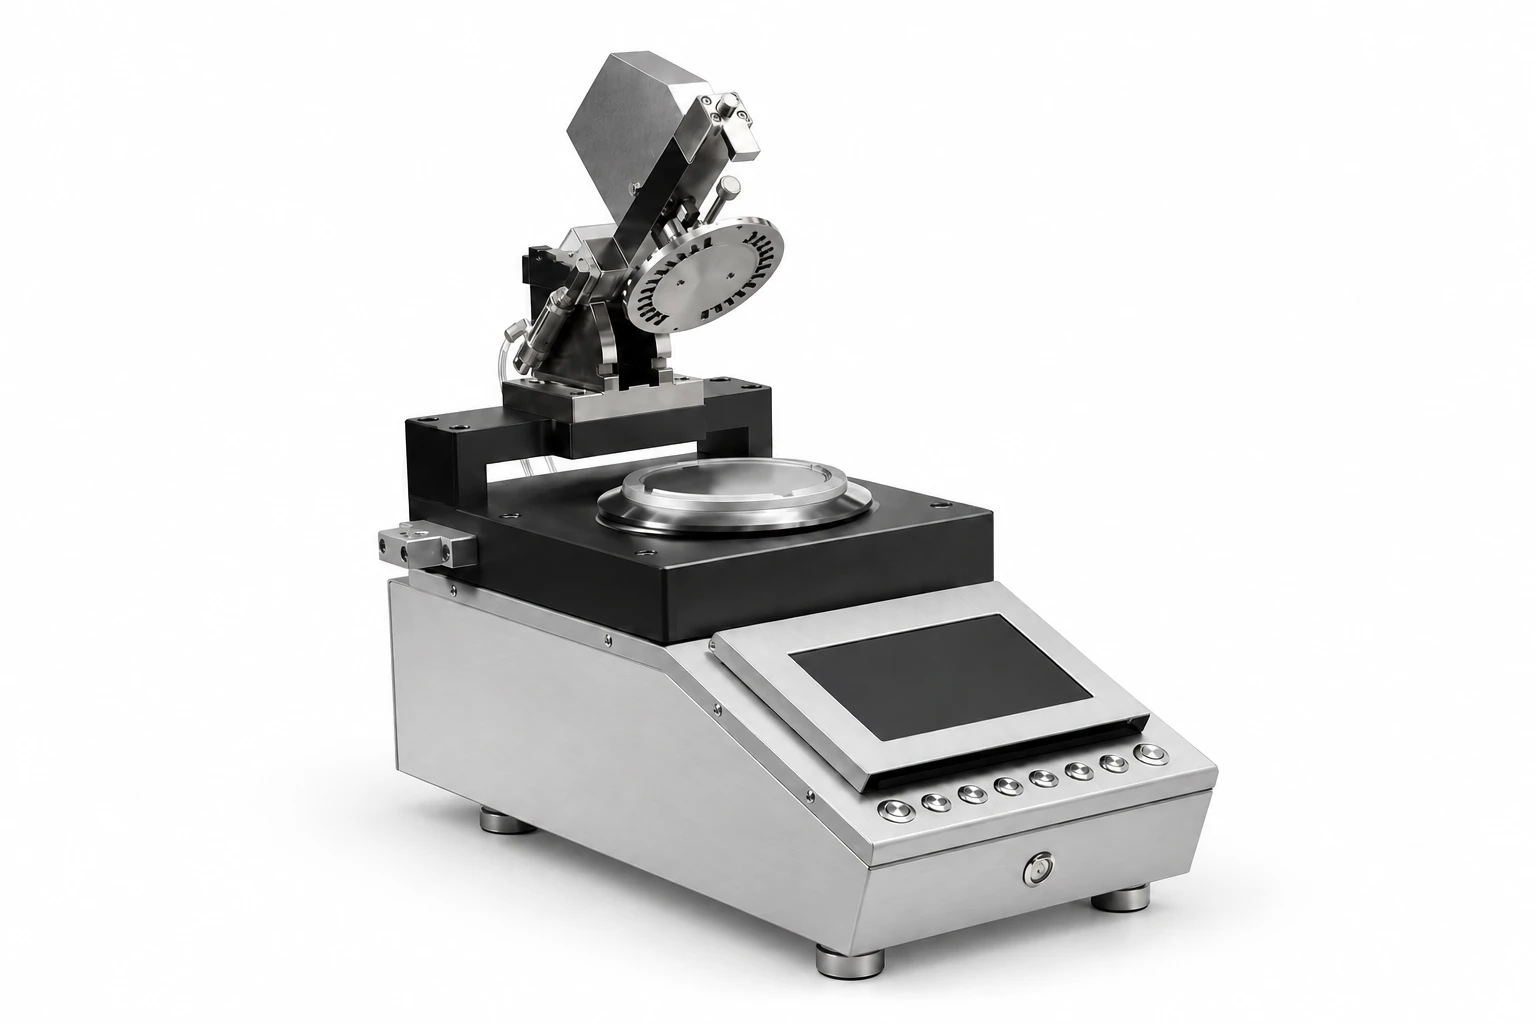
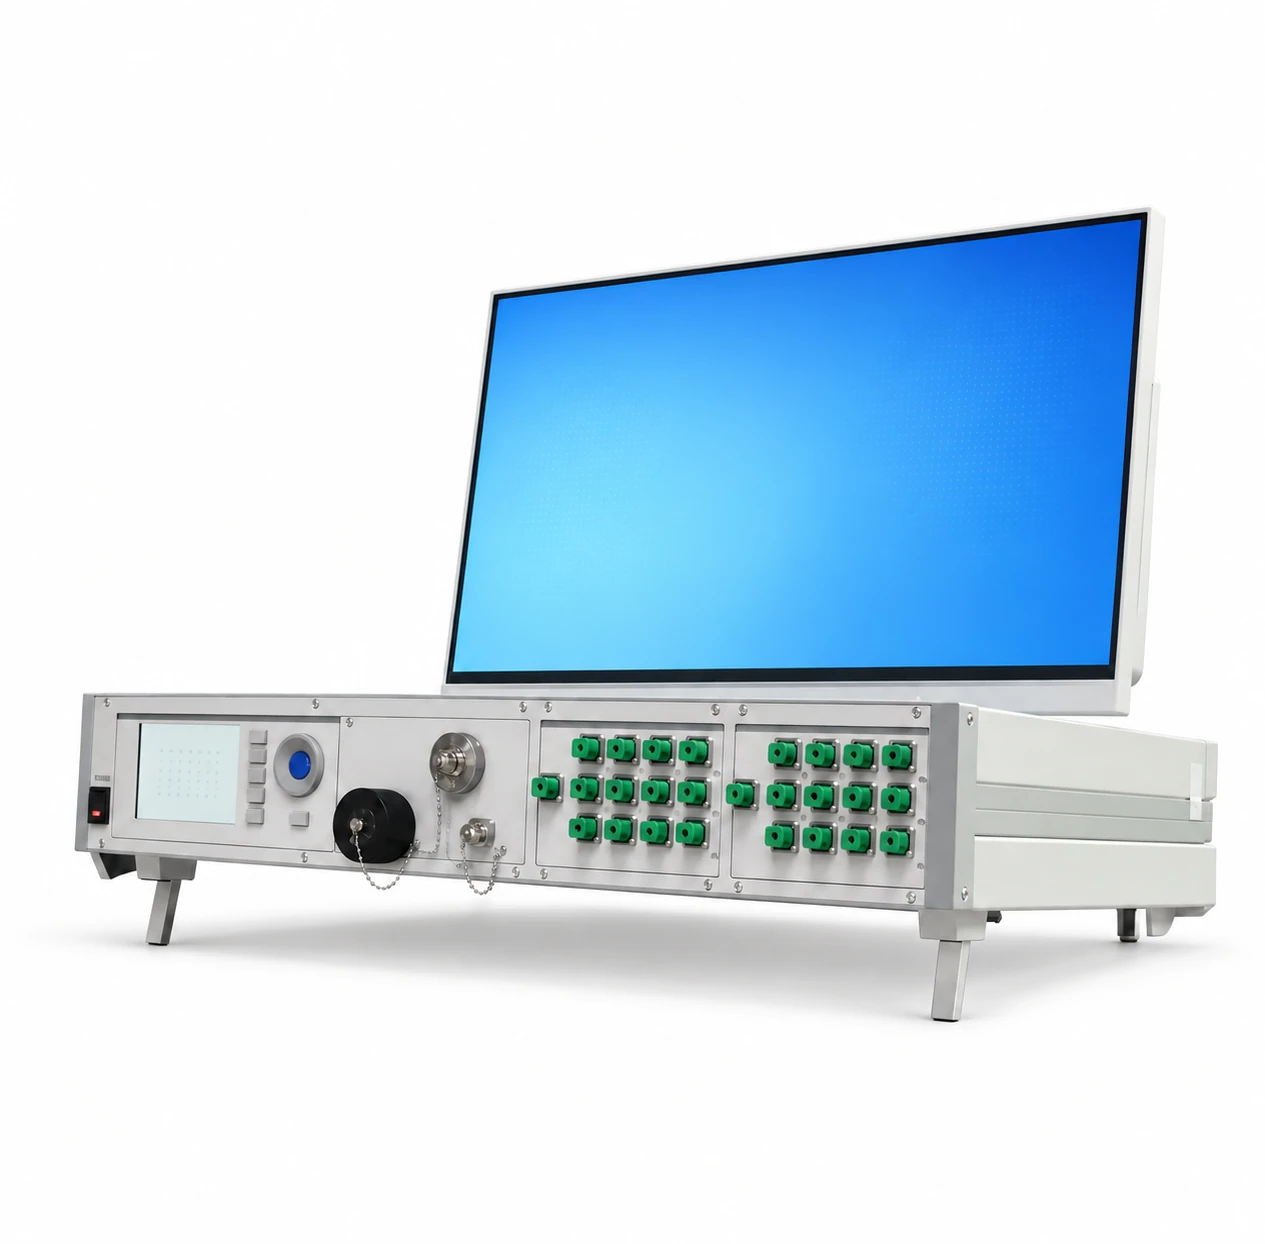
Define cleanliness, handling, ESD where applicable and storage conditions from the selected process. No generic cleanroom class is assumed.
Voltage, frequency, connected loads and protection.
Pendinginan jalur, kualitas air, dan sirkulasi ulang.
Udara tekan, ventilasi, dan ekstraksi khusus proses.
Stasiun kerja, label, catatan, dan penyimpanan berkas hasil.
Tata letak akhir mengikuti dimensi bangunan Anda, mesin yang dipilih, dan tinjauan keselamatan. Zona alur kerja ini bukan gambar konstruksi.
08PHASED FACTORY CONFIGURATION
A complete factory can be planned in phases. Keep one approved launch product and a clear acceptance boundary at each step.
Plan cable manufacturing, cable release, MPO assembly and final testing as one coordinated project.
Best starting point for discussing a complete new factory.
Rencanakan Pabrik MPO Saya09PROJECT SCOPE & RESPONSIBILITY
HONGKAI engineers the cable-making route and coordinates specialist MPO assembly, inspection and test equipment. The signed scope defines who supplies, proves and supports each part.
10EXECUTION, FAT & HANDOVER
Milestones are agreed after scope review. Each step has a decision and a deliverable, not a generic lead-time promise.
Launch product, channel map, target output and acceptance plan.
Lini yang disesuaikan, sel kerja, BOM, tata letak, dan matriks tanggung jawab.
Run the purchased route at FAT and retain the linked evidence.
Periksa kesiapan lokasi, lakukan instalasi, dan komisioning lingkup yang telah ditentukan.
Train operators, repeat the agreed checks and close open items.
Ikuti satu rakitan peluncuran yang telah diidentifikasi dari gulungan kabel sumber hingga hasil saluran akhirnya. Sertakan penerimaan tahap kabel dan penerimaan ujung belakang dalam rencana proyek yang sama.
Baca panduan proses lengkapCable drawing, connector system, channel map and test limits.
Hasil kabel, catatan pengawetan, gambar ujung serat, geometri jika ditentukan, dan file uji saluran.
Instruksi kerja yang dapat diulang, kontrol resep, pembersihan, pengaturan pengujian, dan perbaikan yang diizinkan.
Request an agreed sample run and evidence package for the scope you are purchasing.
Images on this page are presentation references. They are not a claim that a specific customer factory has been delivered.
11KNOWLEDGE & DECISION SUPPORT
12FREQUENTLY ASKED QUESTIONS
Answers to the questions that change a project’s scope.
Tidak. Pabrik referensi menggabungkan lini produksi kabel lengkap dengan workcell perakitan dan inspeksi MPO presisi. Kabel yang telah dirilis berpindah antara kedua sistem tersebut dengan identitas dan catatan penerimaannya.
Lingkup ini dimulai dengan serat optik yang dibeli. Produksi preform serat optik dan penarikan serat tidak termasuk dalam rute referensi.
Tidak dalam referensi serat 12 yang ditunjukkan di sini. Serat-serat yang dilapisi buffer ketat secara individual membentuk inti kabel berbundel. Susunan linear serat dibentuk selama persiapan konektor MPO sesuai dengan peta saluran yang telah disetujui.
Kategori dan jumlah serat, konstruksi kabel, barisan ferrule, jenis kelamin (gender), orientasi kunci, polesan, polaritas, serta persyaratan pengujian menentukan mesin, perlengkapan, dan adaptor yang kompatibel. Setujui perluasan untuk produk mendatang yang telah disebutkan.
Keduanya merupakan bagian dari pembahasan lingkup, bukan termasuk secara otomatis. BOM yang ditandatangani dan matriks tanggung jawab mengidentifikasi material yang disediakan, dukungan pengadaan, instrumen laboratorium kabel, pengujian perakitan oleh spesialis, serta semua item yang disediakan pembeli.
Ya, itu merupakan opsi perencanaan. Mulailah dengan kabel yang dibeli dan telah memenuhi syarat serta rute pelepasan perakitan yang disepakati, lalu evaluasi buffering dan jaket dalam rumah sebagai fase ekspansi terpisah. Kapasitas dan kompatibilitas masih perlu ditinjau.
MPO adalah keluarga antarmuka konektor. MTP® merupakan merek US Conec dari konektor MPO. Ruang lingkup pabrik MPO generik tidak menetapkan pasokan komponen, otorisasi, atau kompatibilitas MTP; sebutkan sistem konektor dalam ringkasan proyek.
Capacity, floor space and delivery time are confirmed from your launch-product mix, target output, shifts, validated cycle times, equipment arrangement, utilities and site readiness. The agreed configuration defines the project-specific figures.
13YOUR MPO FACTORY PROJECT
Buat ringkasan proyek seputar produk MPO Anda, target produksi, dan lokasi. Biarkan spesifikasi yang belum diputuskan terbuka untuk ditinjau oleh tim teknik.
Review your brief before sending it to HONGKAI. Nothing is sent automatically.
Your cable drawing, connector specification and factory floor plan. You can share these during the technical follow-up.
 English English
 Русский
 हिन्दी
 한국어
 বাংলা
 Bahasa Indonesia
 Tiếng Việt
 മലയാളം
 Português do Brasil
 العربية
 فارسی