

Cable release
Manufacture and release the MPO base cable.
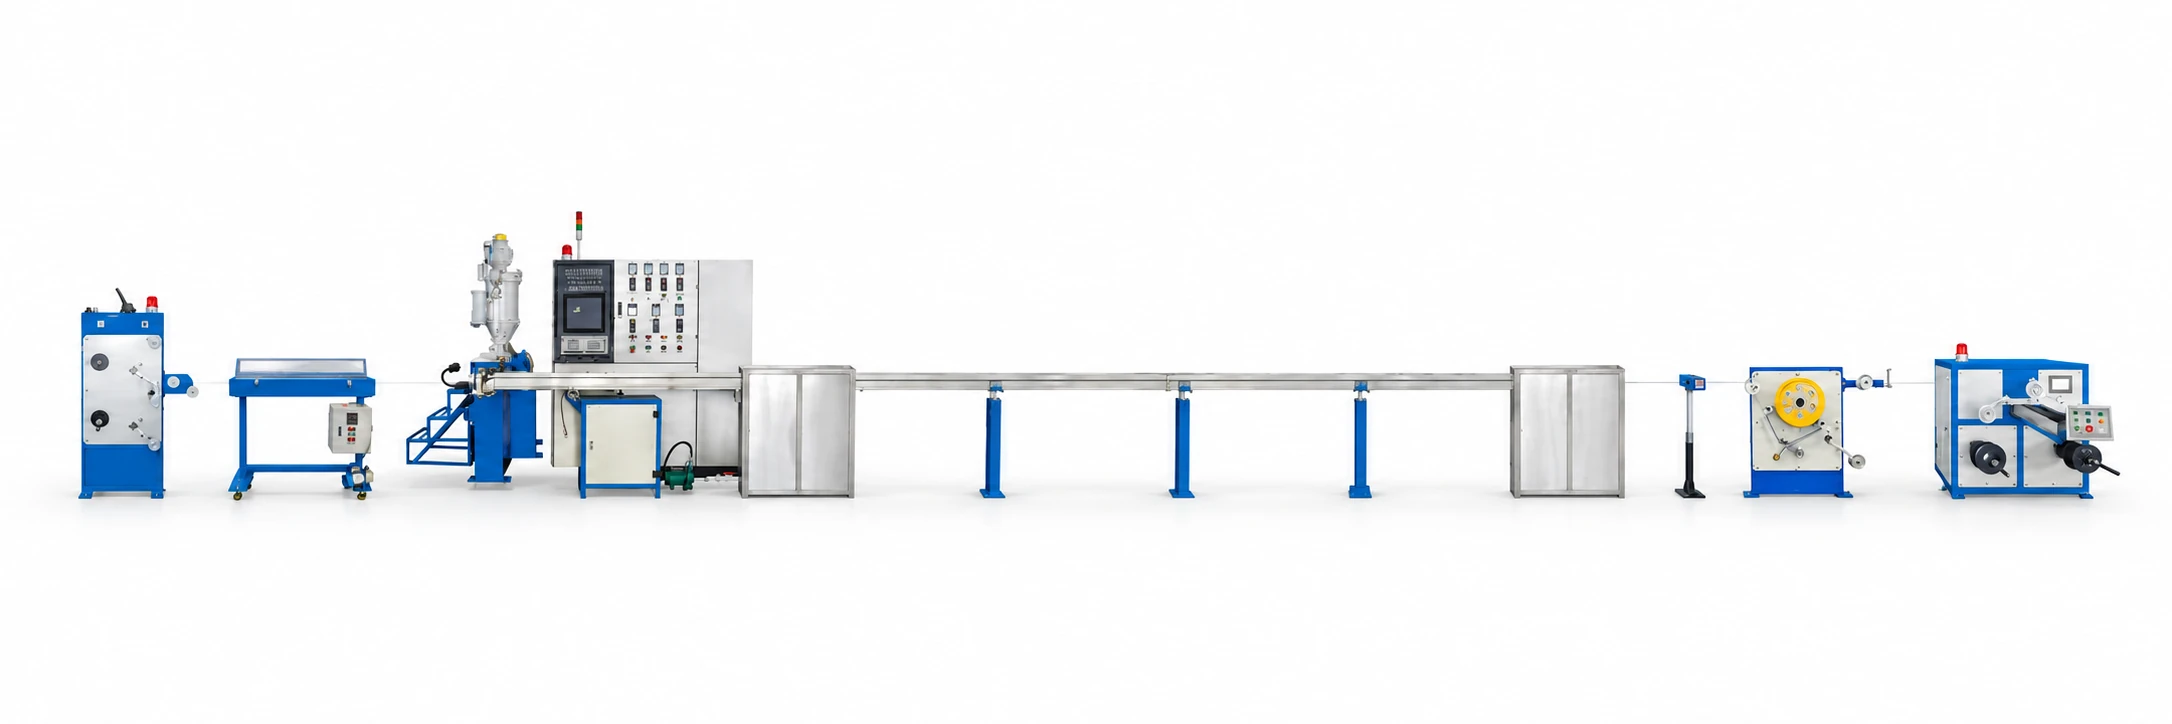
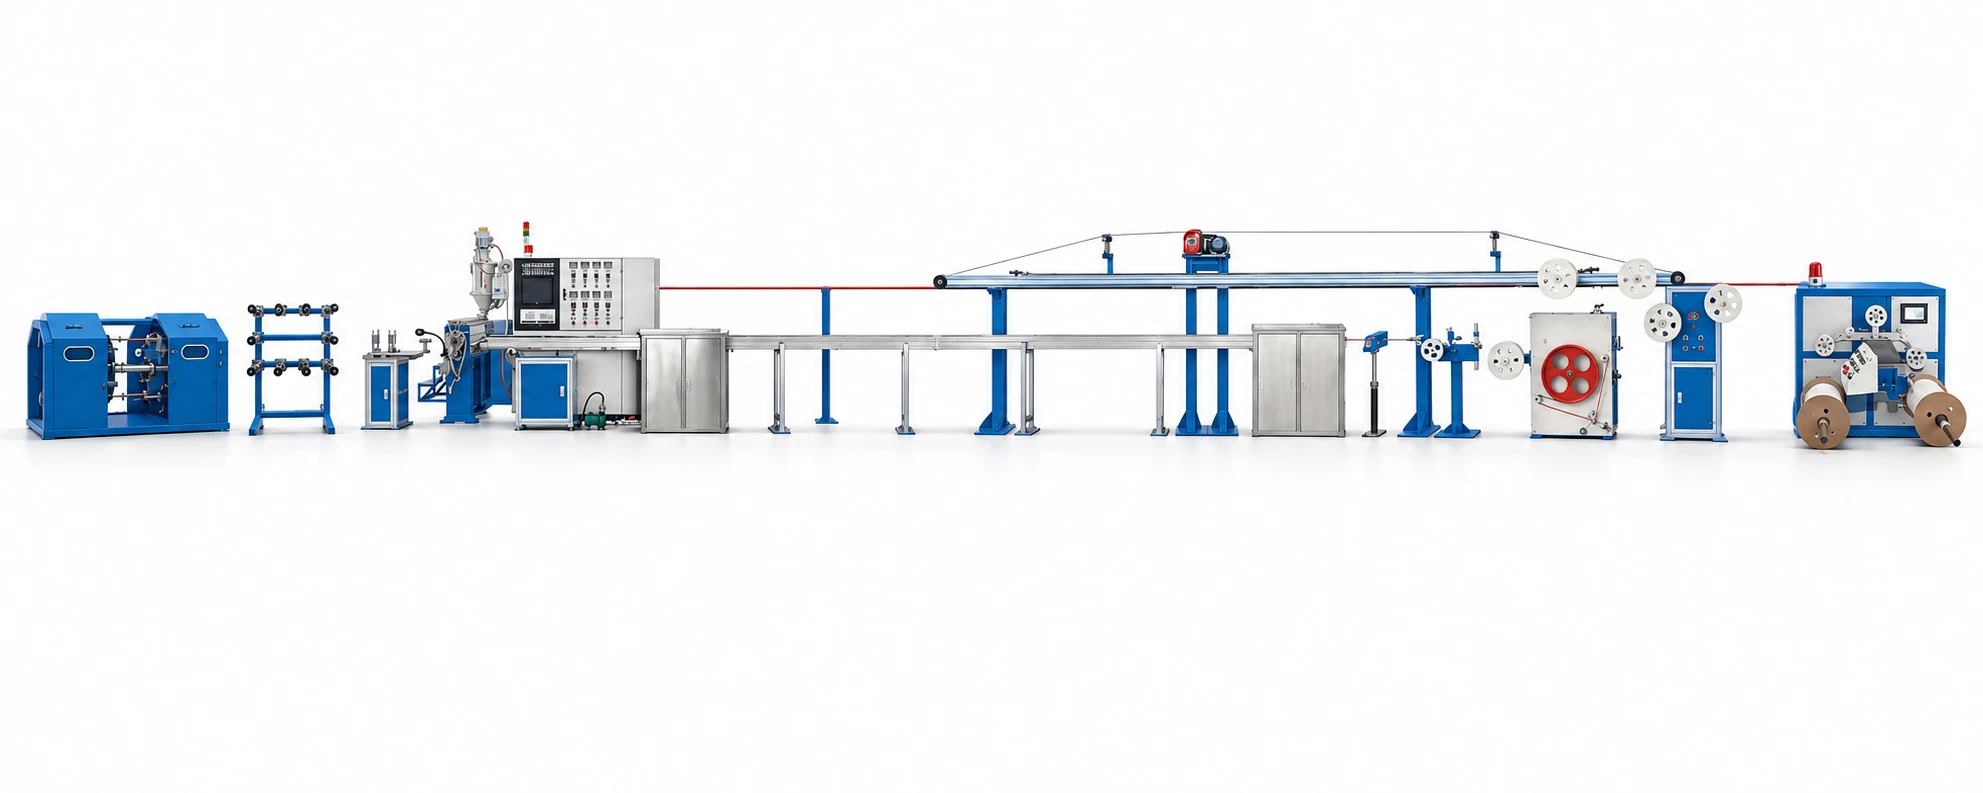
- HK-30 buffering and configured GJFJV jacketing
- Verified cable structure, dimensions and fiber identification
- Optical and agreed mechanical release records
MPO CABLE & ASSEMBLY FACTORY SOLUTION
From optical fiber to a tested MPO assembly.
A complete factory solution with equipment, materials, layout and know-how for cable manufacturing and precision MPO assembly.
For new factories, existing cable manufacturers and assembly businesses ready to expand.
Plan My MPO FactoryExplore the full process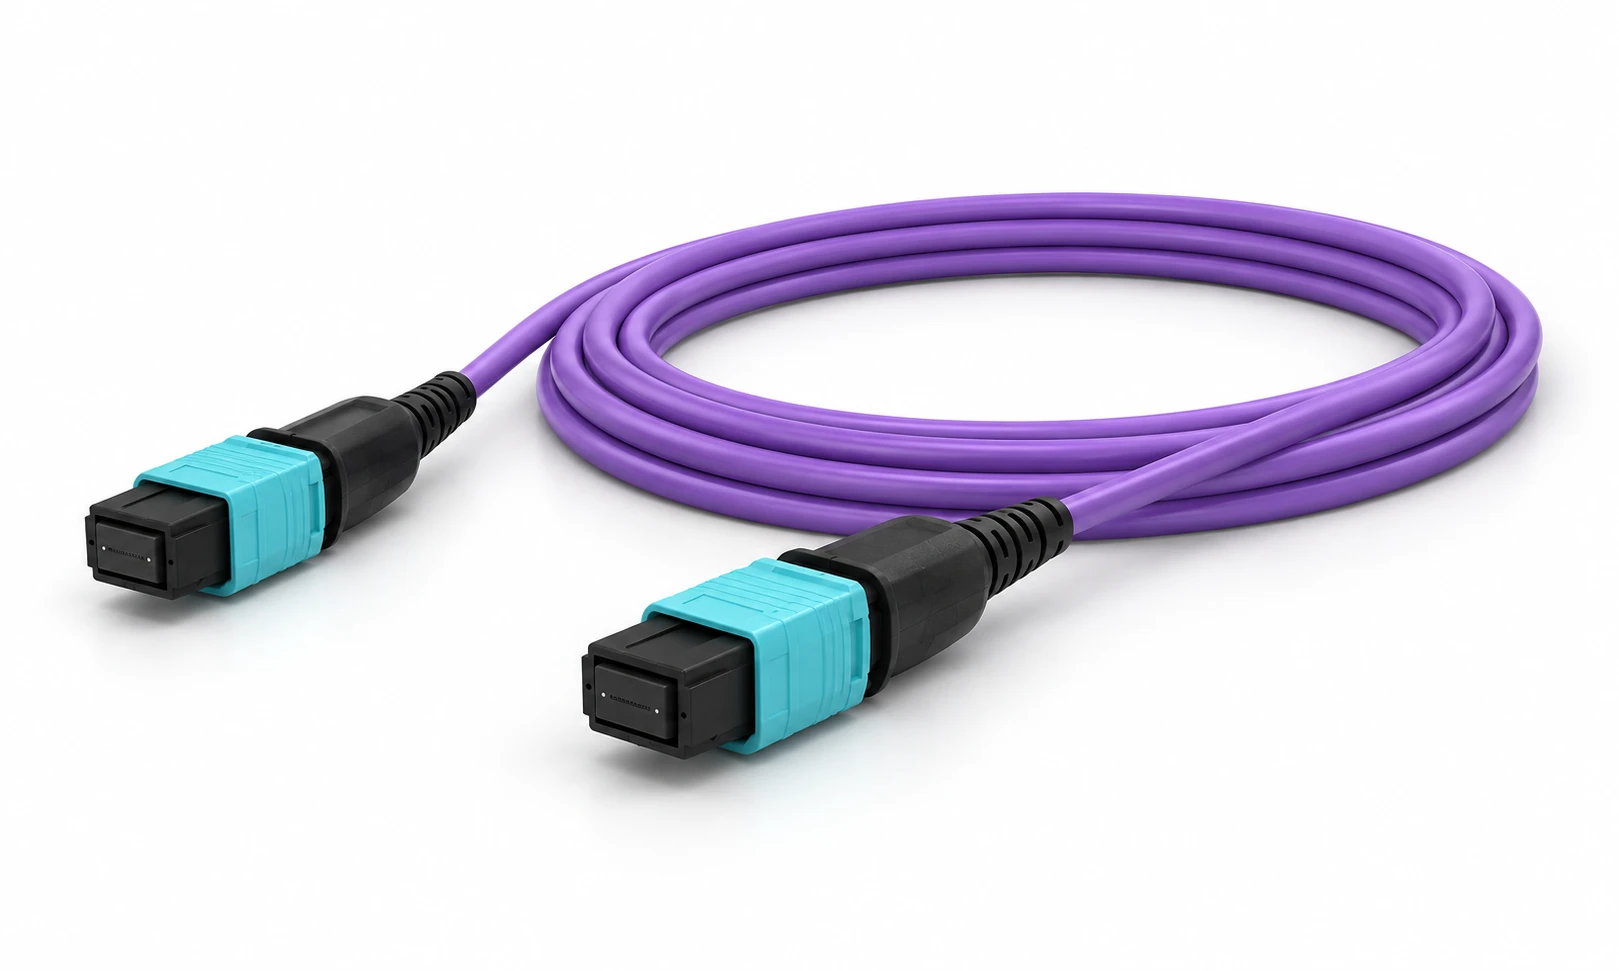
Illustrative reference.
Final scope follows the
approved product.
INTERACTIVE PROCESS EXPLORER
See what to make, which areas are required, and how each step fits into a complete MPO factory.
STAGE 04 / 07
Individual fibers are separated, identified and arranged into a linear array for MPO termination.
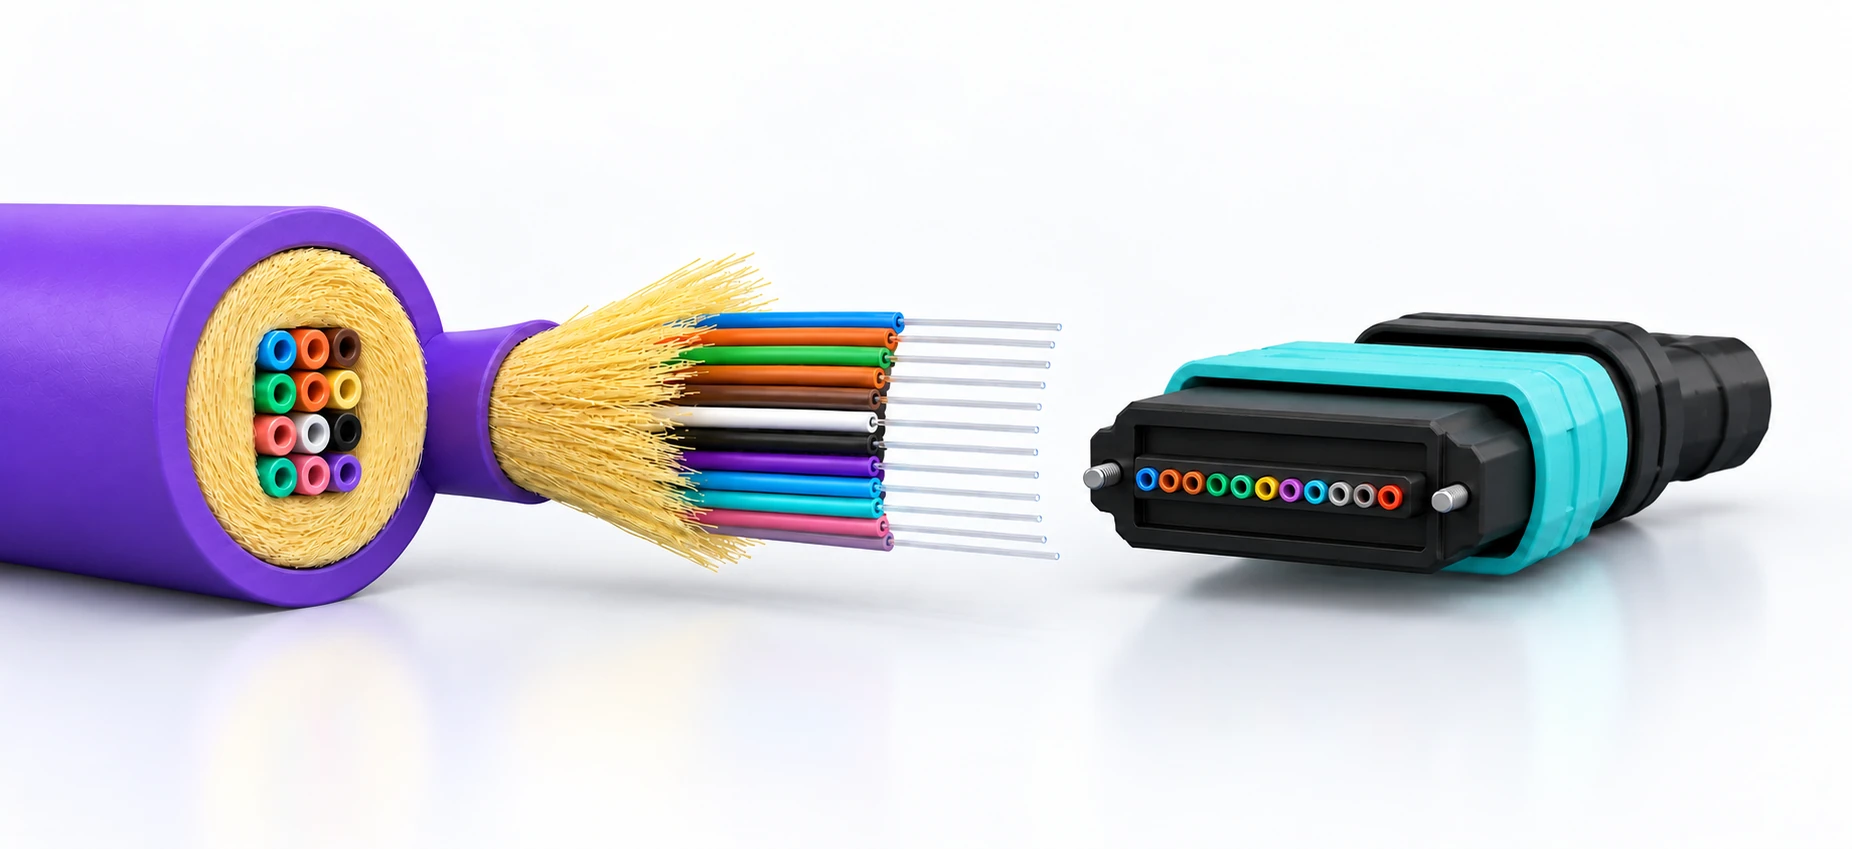
31 operations and control points across seven stages. Open a stage for its full scope.
Before production: approve the launch assembly, cable drawing, fiber category and count, connector rows, gender, key orientation, polish, channel map and acceptance plan. The signed work instruction controls the exact sequence.
Confirm fiber identity, specification, coating compatibility, material lots and the incoming optical baseline.
Fiber pay-off → configured preparation → buffer extrusion → cooling → dimensional monitoring → traction and take-up. Identify each finished reel.
Follow the approved cable drawing and feeding order. This reference forms a bundled core, not a flat ribbon. Confirm the gathering-cage interface.
Match the yarn packages, guides and controlled tension to the approved construction.
Common-jacket extrusion → cooling → diameter monitoring → capstan and take-up. Link the finished reel to fiber, yarn and polymer lots.
Verify construction, dimensions, identification, continuity and the agreed optical results against the cable control plan.
Scope tensile, crush, bend and temperature checks with the agreed methods and sampling plan. Cable-laboratory instruments are separate from online gauges and MPO testers.
Retain cable-stage acceptance records. Carry the source-reel identity into every measured and cut assembly length.
Cut to the approved assembly length and branch plan. Carry source-reel identity to each piece. This operation is required even without a separately quoted cutting machine.
Expose the specified fiber length and prepare the strength members without damage. Follow the cable and connector preparation instructions.
Place the specified boots and hardware on the cable in the connector-defined order before later operations prevent access. Verify the component set against the assembly BOM.
Use thermal stripping only with a compatible fiber/coating and approved instruction. Check stripped length and fiber damage.
Identify and place each fiber in its approved linear position. The arranger does not choose or create polarity.
Use a holder matched to fiber count, pitch and material. Recheck order after clamping and retain an identified array record.
Check the selected ferrule, adhesive, process liquids, shelf life, preparation and working time. The work instruction determines the adhesive-and-fiber loading sequence.
Use centrifugal degassing only when required by the material instruction. Link the batch, usable-life status and preparation cycle to the ferrules.
The quoted suction unit is not a universal filling method. Confirm its use, settings and verification with the connector and material instructions.
Confirm ferrule lot, orientation and loaded-array order. This is a required operation; the reference equipment list does not establish a separate powered loader.
Use the qualified adhesive recipe. Record holder, batch, load, time-temperature evidence and post-cure inspection. Oven quantity alone does not prove capacity.
Perform at the connector-defined point, which may differ from this overview order. Prove matched jaws and tooling with the actual housing and aramid arrangement.
Use the connector-approved preparation method and revision. Check the identified ferrule before it enters the polishing route.
Define the removal boundary and whether scraping is normal production or permitted rework. Keep before/after evidence and a damage check.
Match ferrule and polish geometry. The referenced 24-position fixture counts holding positions, not fibers or guaranteed output.
Control load, time, films, pads, cloths, liquids and the cleaning sequence. Retain recipe revision, consumable lots and permitted rework history.
Include only after confirming the processed object, liquid, timing and compatibility. It is not an automatic cleaning step for every MPO assembly.
Use the approved cleaning method and handling controls. Protect the finished surface and pass the identified assembly to inspection.
Use a qualified MPO adapter. Retain identified full-array images and the clean → re-inspect → disposition record. Visual inspection does not replace geometry or optical tests.
Apply the agreed attributes, limits and inspection plan. Retain raw reports, adapter/reference identity and repeatability evidence.
Check both ends against the signed channel map, gender and key orientation. The tester detects mapping errors; it does not correct them.
Match wavelengths, metrics, directions, references and limits to the product. The quoted system is a multimode reference; single-mode and return-loss needs require separate scope review.
Link the final assembly to its source reel, component lots and channel-level results. Fit protective caps and retain the release and packaging record.
Shell removal is rework only unless the connector instruction explicitly states otherwise. Confirm housing compatibility and use limits. After permitted reassembly or rework, repeat the required inspection, polarity and optical checks. Retain the original failed result as well as the repeat results.
COMPLETE FACTORY FLOW
Separate manufacturing and assembly areas.
Clear release points. Connected production records.
Manufacture and release the MPO base cable.
Complete, test and release finished MPO assemblies.
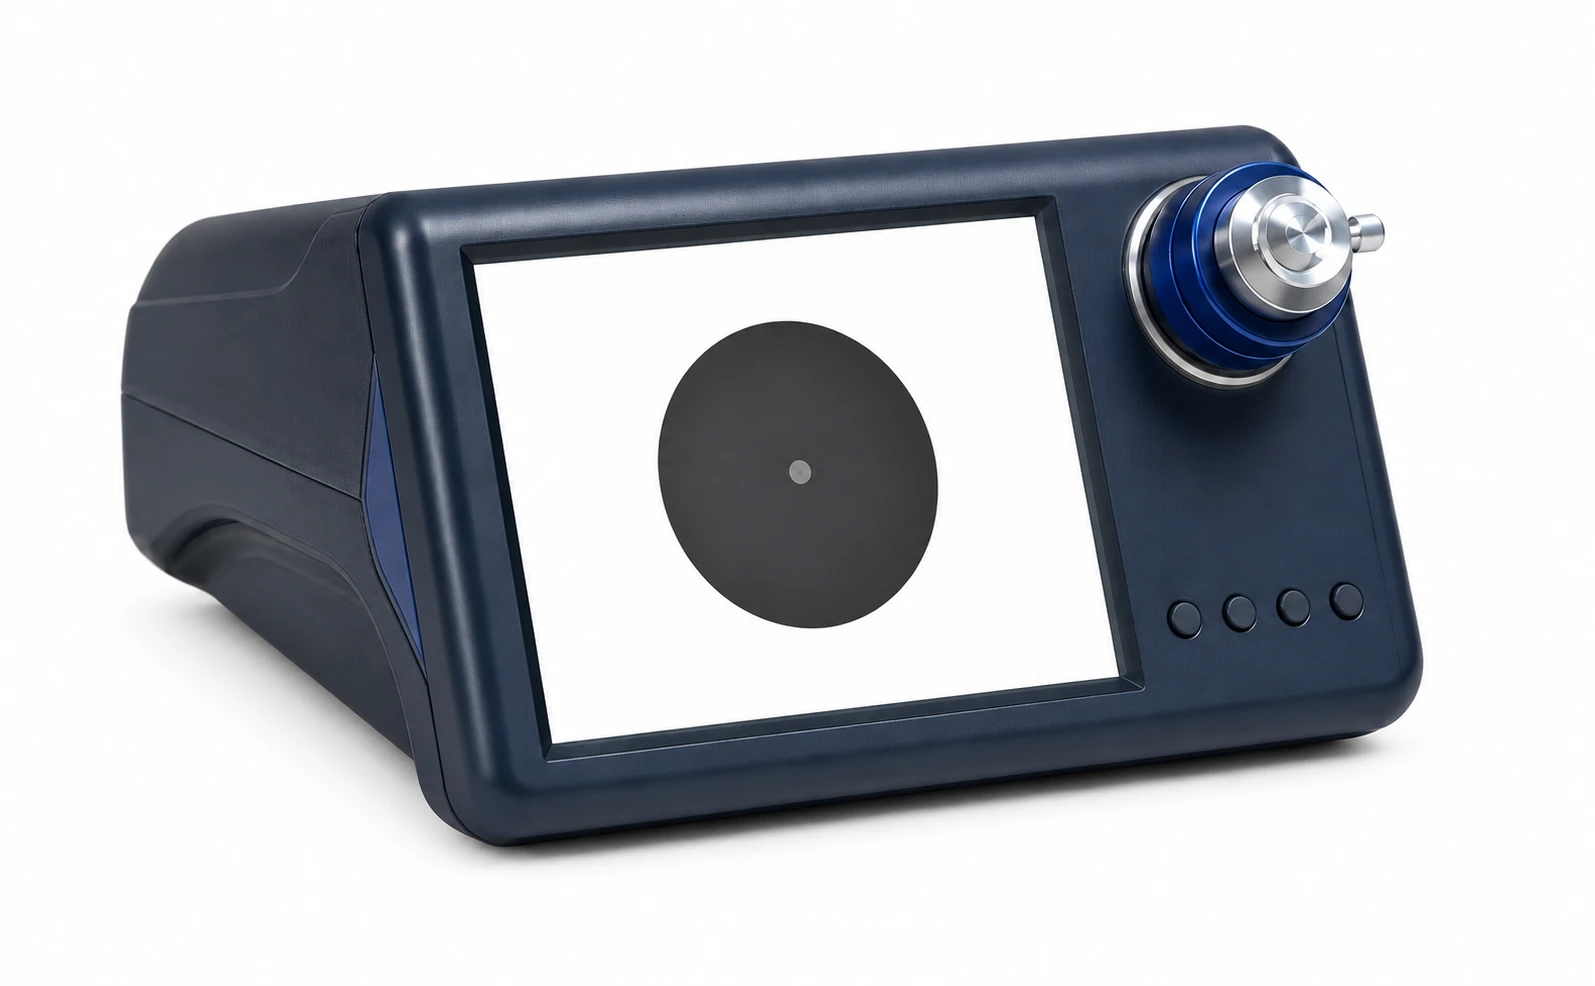
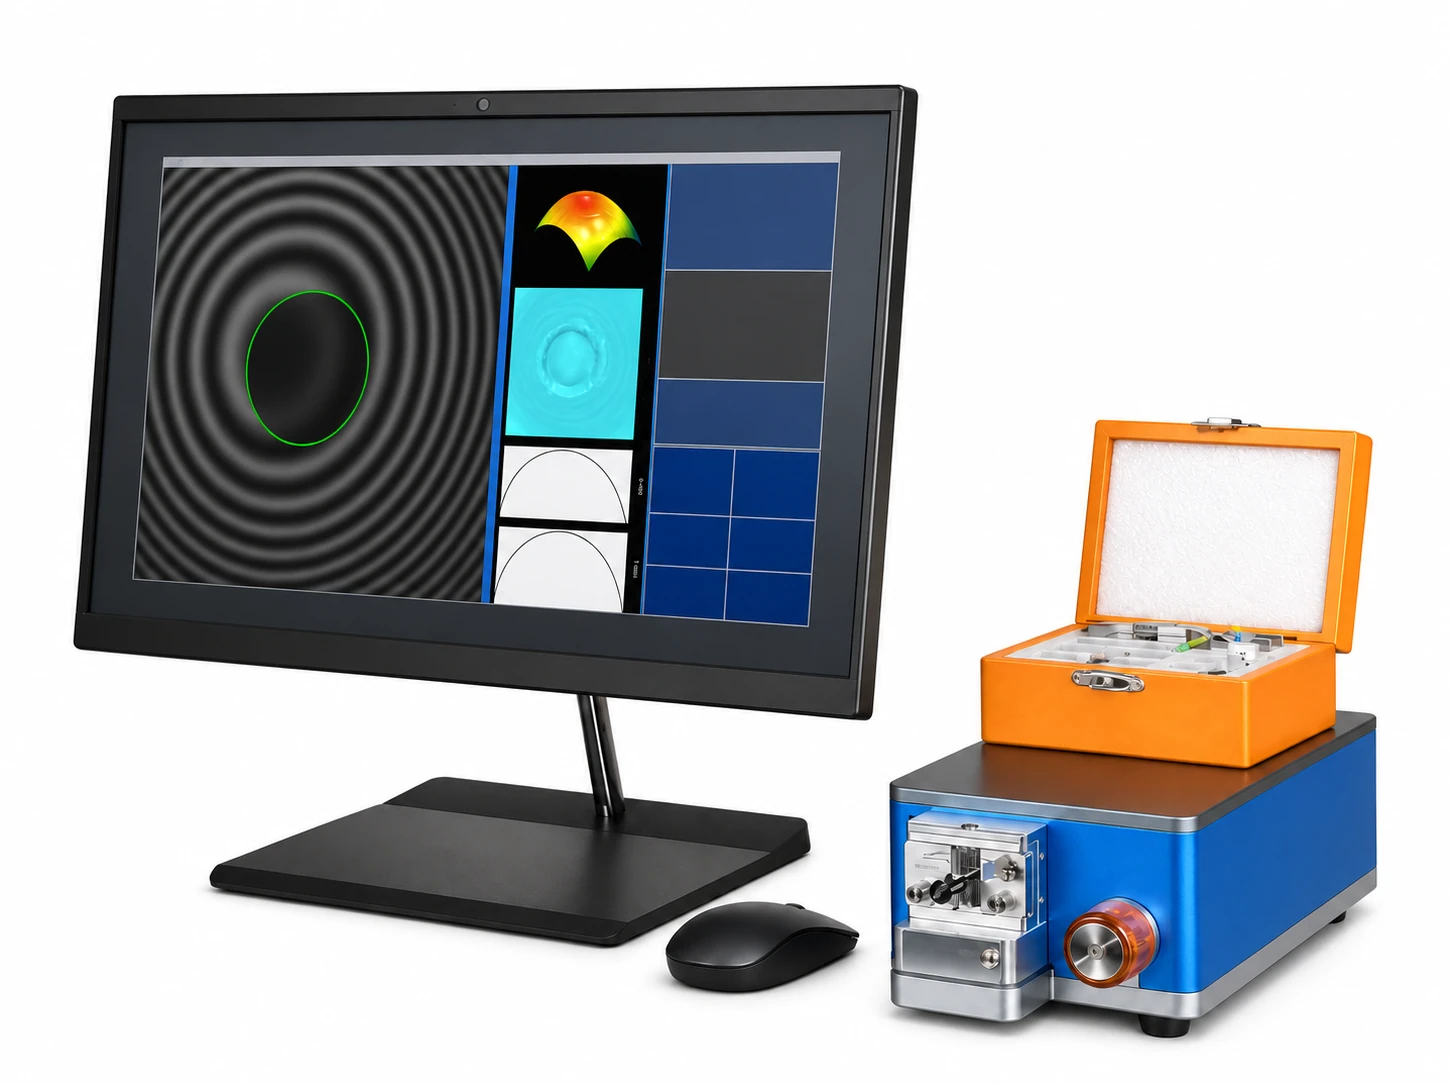
One assembly identity. Keep the link from input fiber reel to finished cable reel, cut length, component lots, ferrule, cure and polishing recipe, inspection images and channel results.
Retain failed and reworked records. An optical pass does not replace the base cable’s own acceptance evidence.
The first decision is your launch assembly. It defines the cable construction, connector workcells and evidence needed for release.
Build your project briefThe illustrated launch example is a 12-fiber GJFJV-type cable feeding MPO assembly. Other constructions require a matched route.
Complete cable lines, specialist assembly tools and separate release instruments.
“Launch route” refers to this reference product, not every MPO design. Equipment renders are configuration references, not a customer-delivery record.
RAW MATERIALS & INITIAL BOM SUPPORT
Plan the cable inputs, connector components and process consumables together, so the first production run has a complete material path.
Match material grades to the cable drawing and process window before sizing the first production batch.
Explore cable materials
Fiber category, coating compatibility, reel identity and incoming checks.
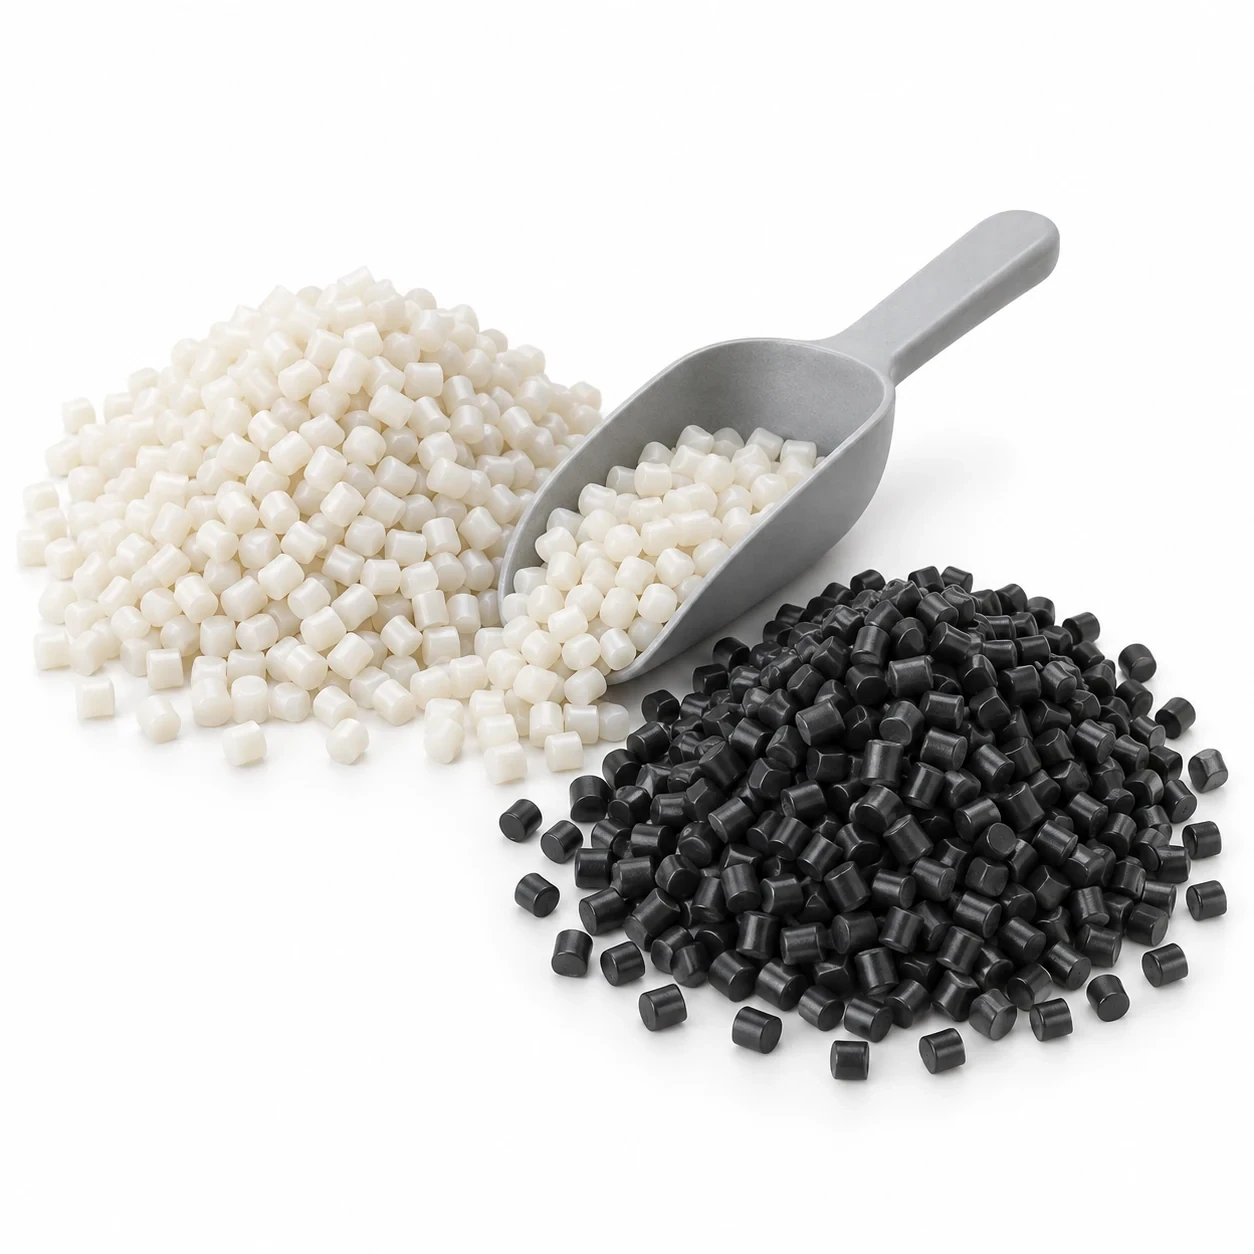
Separate tight-buffer and outer-jacket grades; agree processing and storage conditions.

Construction, linear density, tension range and package compatibility.
Illustrative material references. Exact parts, grades and consumables follow the approved product and process.
Material specifications, supplier review, sample checks and an initial cable BOM.
Connect material flow. Separate heavy cable-making work from precision connector assembly.
Plan machine lengths, service access, reel routes, lifting and safe aisles around the confirmed equipment.

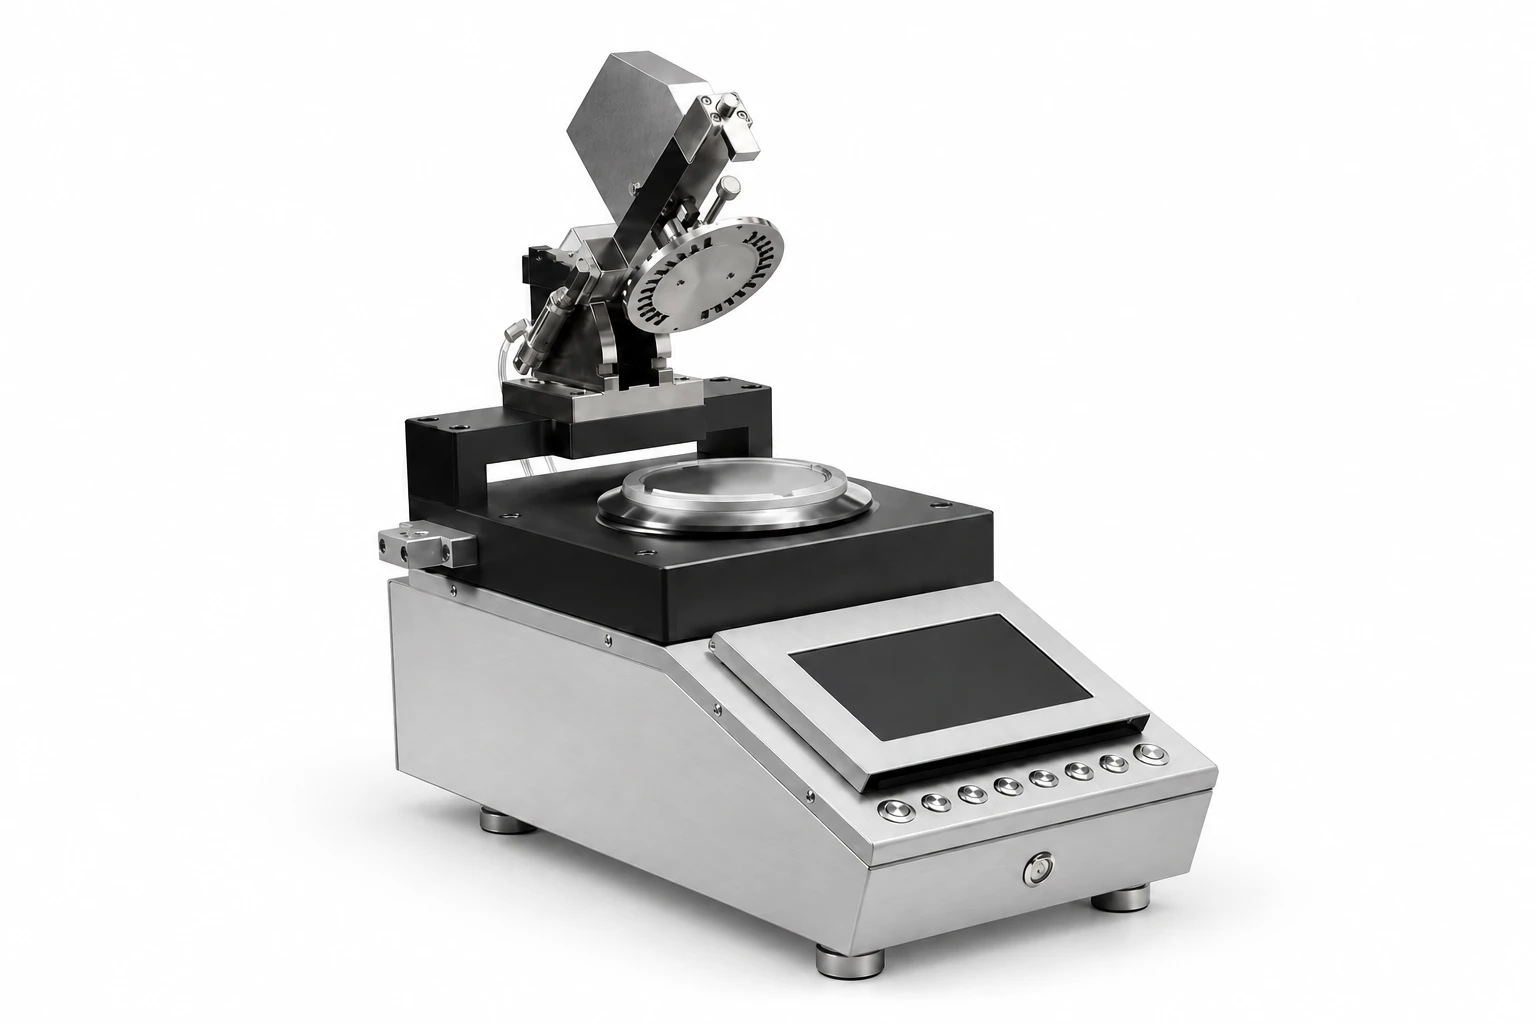
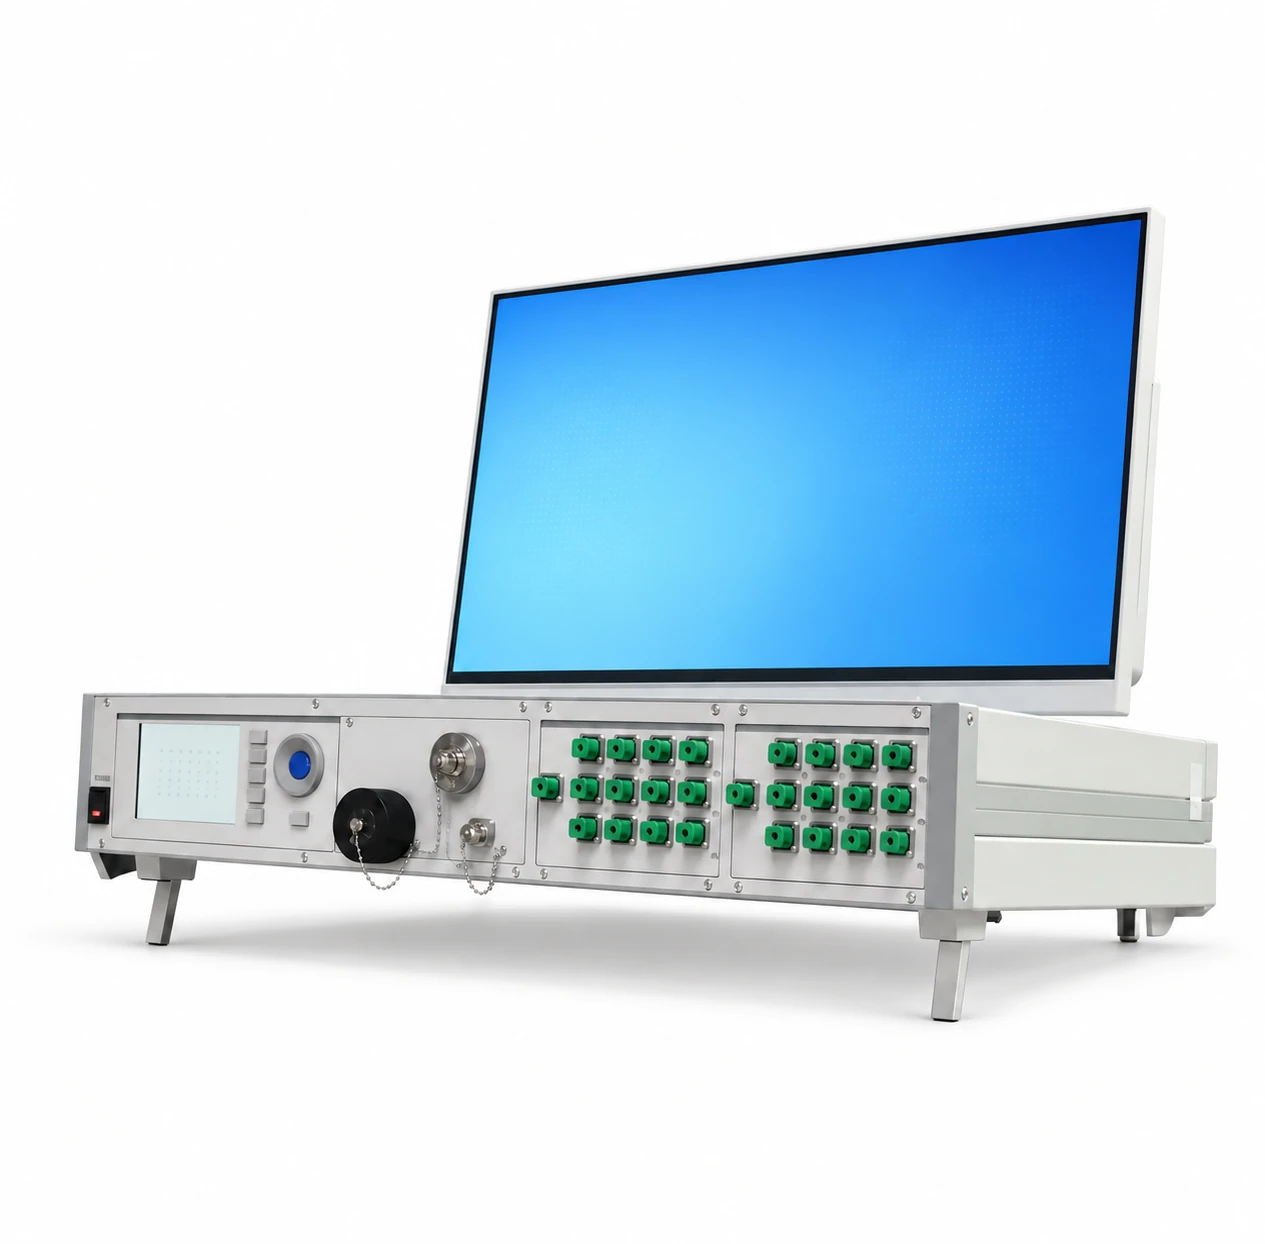
Define cleanliness, handling, ESD where applicable and storage conditions from the selected process. No generic cleanroom class is assumed.
Voltage, frequency, connected loads and protection.
Line cooling, water quality and recirculation.
Compressed air, ventilation and process-specific extraction.
Workstations, labels, records and result-file storage.
A final layout follows your building dimensions, selected machinery and safety review. These workflow zones are not a construction drawing.
A complete factory can be planned in phases. Keep one approved launch product and a clear acceptance boundary at each step.
Plan cable manufacturing, cable release, MPO assembly and final testing as one coordinated project.
Best starting point for discussing a complete new factory.
Plan My MPO FactoryHONGKAI engineers the cable-making route and coordinates specialist MPO assembly, inspection and test equipment. The signed scope defines who supplies, proves and supports each part.
Milestones are agreed after scope review. Each step has a decision and a deliverable, not a generic lead-time promise.
Launch product, channel map, target output and acceptance plan.
Matched lines, workcells, BOM, layout and responsibility matrix.
Run the purchased route at FAT and retain the linked evidence.
Check site readiness, install and commission the defined scope.
Train operators, repeat the agreed checks and close open items.
Follow one identified launch assembly from the source cable reel to its final channel results. Include cable-stage and back-end acceptance in the same project plan.
Read the complete process guideCable drawing, connector system, channel map and test limits.
Cable results, cure record, end-face images, geometry when specified and channel test files.
Repeatable work instructions, recipe control, cleaning, test setup and permitted rework.
Request an agreed sample run and evidence package for the scope you are purchasing.
Images on this page are presentation references. They are not a claim that a specific customer factory has been delivered.
Answers to the questions that change a project’s scope.
No. The reference factory combines complete cable-making lines with precision MPO assembly and inspection workcells. Released cable moves between those two systems with its identity and acceptance records.
This scope starts with purchased optical fiber. Optical-fiber preform production and fiber drawing are not included in the reference route.
Not in the 12-fiber reference shown here. Individually tight-buffered fibers form a bundled cable core. The linear fiber array is formed during MPO connector preparation against the approved channel map.
No. Fiber category and count, cable construction, ferrule rows, gender, key orientation, polish, polarity and test requirements determine compatible machinery, fixtures and adapters. Approve expansion for named future products.
Both are part of the scope discussion, not automatic inclusions. The signed BOM and responsibility matrix identify supplied materials, sourcing support, cable-laboratory instruments, specialist assembly tests and any buyer-supplied items.
Yes, that is a planning option. Start with qualified purchased cable and the agreed assembly-release route, then evaluate in-house buffering and jacketing as a separate expansion phase. Capacity and compatibility still require review.
MPO is the connector interface family. MTP® is a US Conec brand of MPO connector. A generic MPO factory scope does not establish MTP component supply, authorization or compatibility; name the connector system in the project brief.
From the launch-product mix, target output, shifts, cycle validation, equipment arrangement, utilities and site readiness. This page intentionally does not state a universal speed, footprint, yield or delivery schedule.
Build a project brief around your MPO product, production target and site. Leave undecided specifications open for engineering review.
Review your brief before sending it to HONGKAI. Nothing is sent automatically.
Your cable drawing, connector specification and factory floor plan. You can share these during the technical follow-up.


