HK-90 линия наложения оболочки на оптический кабель
Φ90 mm extrusion · Core pay-off to finished cable take-up
USD 118,900 per set
Quoted configuration: HK-90 PLC+IPC Control Outdoor Optical Cable Sheathing Production Line. Ex-factory delivery; the buyer arranges and pays transport. Final equipment and tooling follow the agreed configuration schedule.
Apply the specified outer sheath around your prepared optical cable core. Configure material feeding, aramid yarn stranding or metal-tape protection as required, extrusion, cooling and take-up as one coordinated production stage.
Coordinate melt delivery, tooling, cooling and traction around the cable design.
REFERENCE ARRANGEMENTEquipment quantities and final layout follow the reviewed project.
Scope boundary: this page covers the sheathing stage. Upstream coloring, loose-tube extrusion and SZ core stranding are separate processes. Reinforcement and armoring modules are selected for the approved cable construction.
02PROCESS & MATERIAL HANDOFF
From prepared core to finished outer sheath.
Build the process around the cable layers. Optional protection modules are selected before the extrusion and downstream handling requirements are finalized.
01CORE & MATERIAL PAY-OFF
Feed the specified construction.
Start with the prepared core or loose tube. Match the core, wire and protection-material pay-offs to the incoming package.
02PROTECTION & FORMING
Prepare the layers before extrusion.
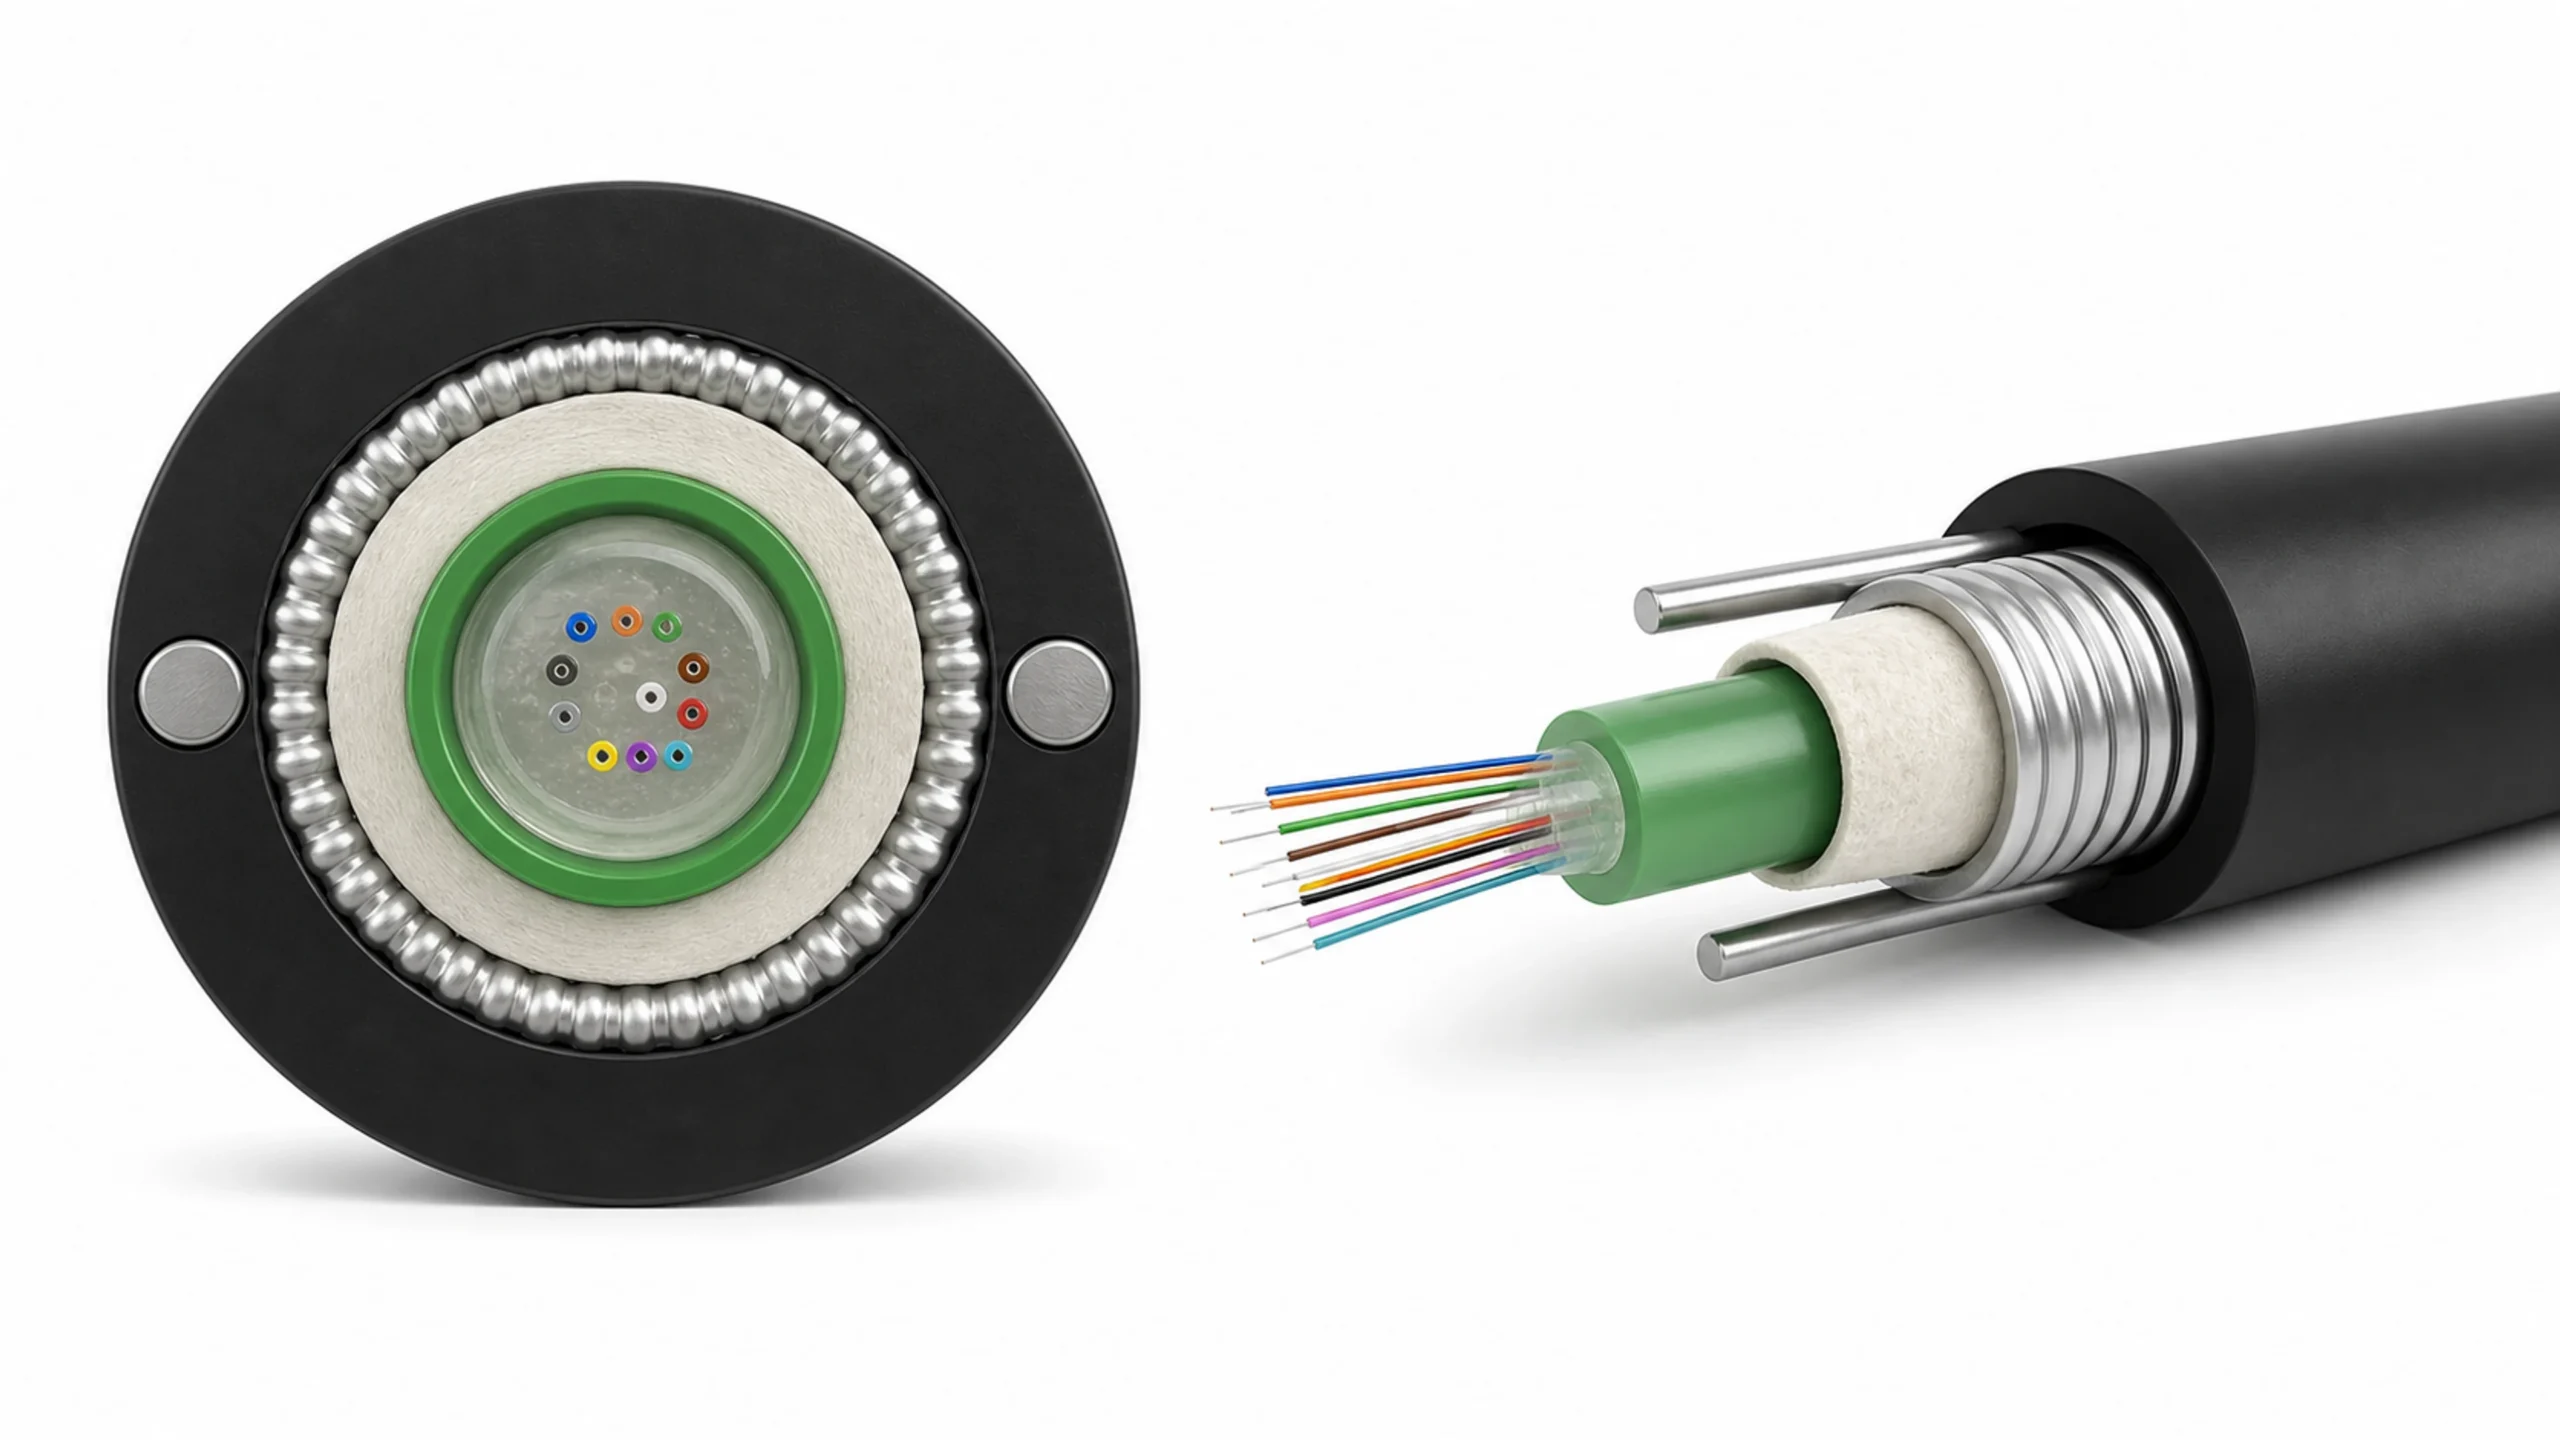
Apply the selected water blocking and ripcord. ADSS routes add aramid yarn stranding before the outer sheath; armored routes use the specified metal-tape preparation and forming modules.
03SHEATH EXTRUSION
Form the outer jacket.
Feed the approved compound to the Φ90 mm extruder and crosshead. Coordinate melt delivery, cable centering, temperature and line speed.
04COOLING TO TAKE-UP
Cool, inspect and collect.
Cool and dry the sheath, monitor diameter, apply the specified marking and tests, then coordinate caterpillar traction with finished-cable take-up.
3DINTERACTIVE LINE VIEW
Explore the line. Inspect each device.
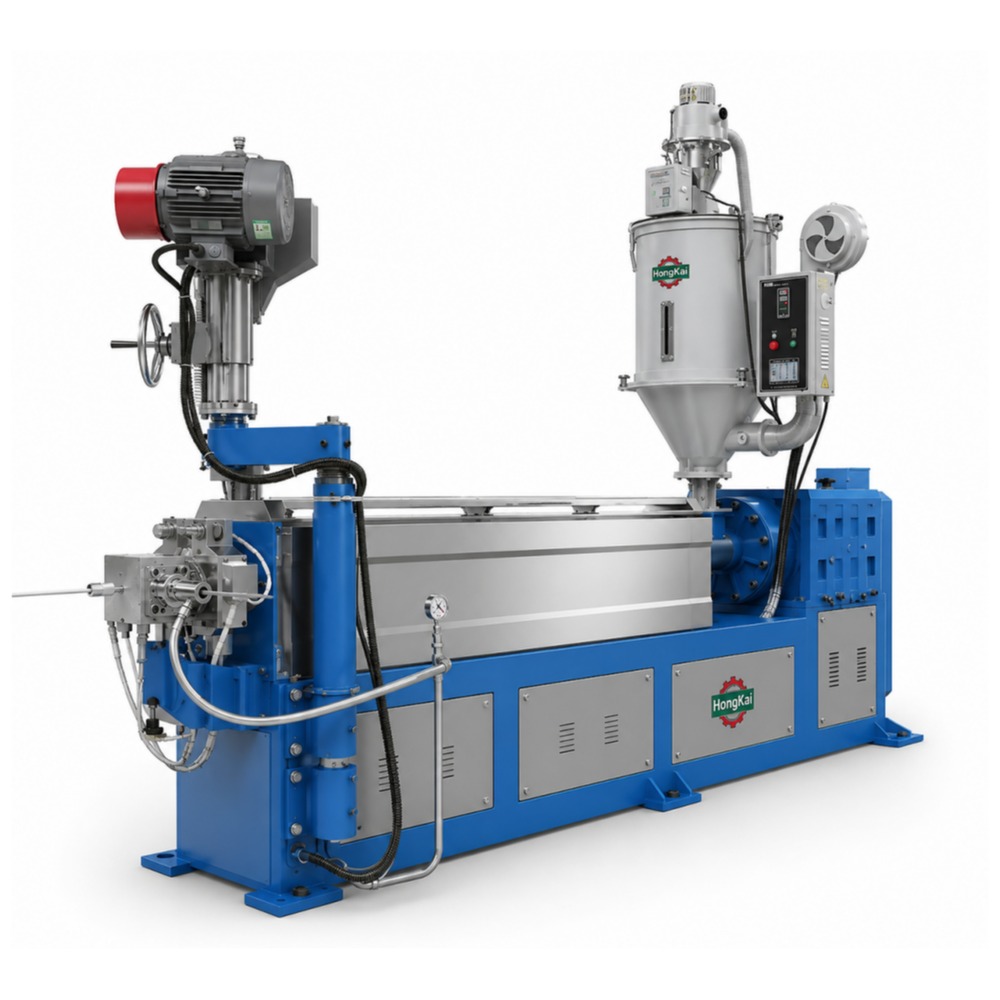
Rotate the HK-90 line, select a device for a closer look, and compare its exterior with the original equipment photograph.
Preparing the interactive line…
The interactive view could not finish loading. Retry the 3D view, or use the equipment references on this page.
Illustrative exterior study. Final equipment, dimensions and layout follow the approved project configuration.
03CONFIGURATION & PROJECT SCOPE
Choose the protection route for your cable.
The same extrusion stage can sit within different process routes. Compare the incoming core, reinforcement and tape requirements before defining the equipment package.
PROJECT EQUIPMENT REFERENCEMetal-tape corrugating unit
CONFIGURATION BASISConstruction-specific modules · final scope by cable drawing
04EQUIPMENT IN THE LINE
Follow the line, one machine at a time.
Select a number or equipment card to see its equipment area, image and process role. Dashed regions identify process interfaces whose final position must be confirmed. The reference includes optional preparation and testing modules; the final equipment list follows your cable construction.
HK-90 EQUIPMENT MAP · REFERENCE ARRANGEMENT
13 - Φ90 mm sheath extruderEquipment area in the reference arrangement
SELECTED EQUIPMENT · PROJECT REFERENCE13 / 23
Equipment shown is for reference. Final construction and quantity follow your approved equipment list.
SHEATH EXTRUSION
Φ90 mm sheath extruder
Plasticizes the approved sheath compound and supplies the adjustable crosshead. The reference uses a Φ90 mm screw with a 25:1 L/D ratio.
CONFIRM FOR YOUR PROJECT
Compound grade, screw and crosshead, tooling, temperature profile, output and required jacket dimensions.
Selected equipment 13: Φ90 mm sheath extruder
Эталонная граница: the panorama illustrates equipment order, not the final machine count, footprint or construction. The approved layout and equipment list define machine quantities, dimensions and the supplied arrangement.
05TECHNICAL CONFIGURATION REVIEW
Define the operating conditions behind the specification.
Use the reference below to begin the technical review. Confirm the complete cable construction, material grade and trial conditions before agreeing production performance.
HK-90 reference data and project confirmation points
Review area
Reference / requirement
Condition to confirm
Extruder reference
Φ90 mm screw · 25:1 L/D · 75 kW main drive.
Reference equipment configuration; screw, crosshead and tooling must suit the compound and cable.
Aramid stranding reference
24 heads · independent tension · adjustable pitch · S or Z lay.
Selected for the cable construction. Confirm yarn grade, quantity, tension and stranding pitch together with extrusion speed. The reference 120 rpm rotation is not a cable line speed.
Sheath materials
PE / PVC for the reference extruder configuration.
Confirm the compound grade and process settings. Other compounds require a separate suitability review.
Скорость производства
Reference: up to 80 m/min for PE cable below Φ10 mm.
Reference value; confirm the complete construction, jacket thickness, cooling, reel changes and quality targets.
Extrusion output
Reference: up to 250 kg/h PE, with the crosshead open.
An extruder-output reference is not guaranteed finished-cable throughput. Verify it with the agreed tooling and compound.
Cable & tooling range
Specify incoming core, finished diameter and jacket thickness.
Review every module. A metal-tape forming tool may have a narrower range than the extruder or capstan.
Reels, tension & utilities
Agree supply/output drums, winding tension, layout and utility loads.
Use one approved schedule for the chosen configuration; do not infer these values from the HK-90 name.
Controls & acceptance
PLC / IPC coordination, recipes, alarms and agreed inspection records.
Define instruments, interfaces, safety functions, trial duration and acceptance criteria.
CABLE DRAWING → TECHNICAL SCHEDULE → ACCEPTANCE
Confirm the technical schedule for your cable.
Review output together with the sheath cross-section, compound, tooling and cooling capacity. Reel capacity, line footprint, tension settings and utility loads are finalized for the selected configuration.
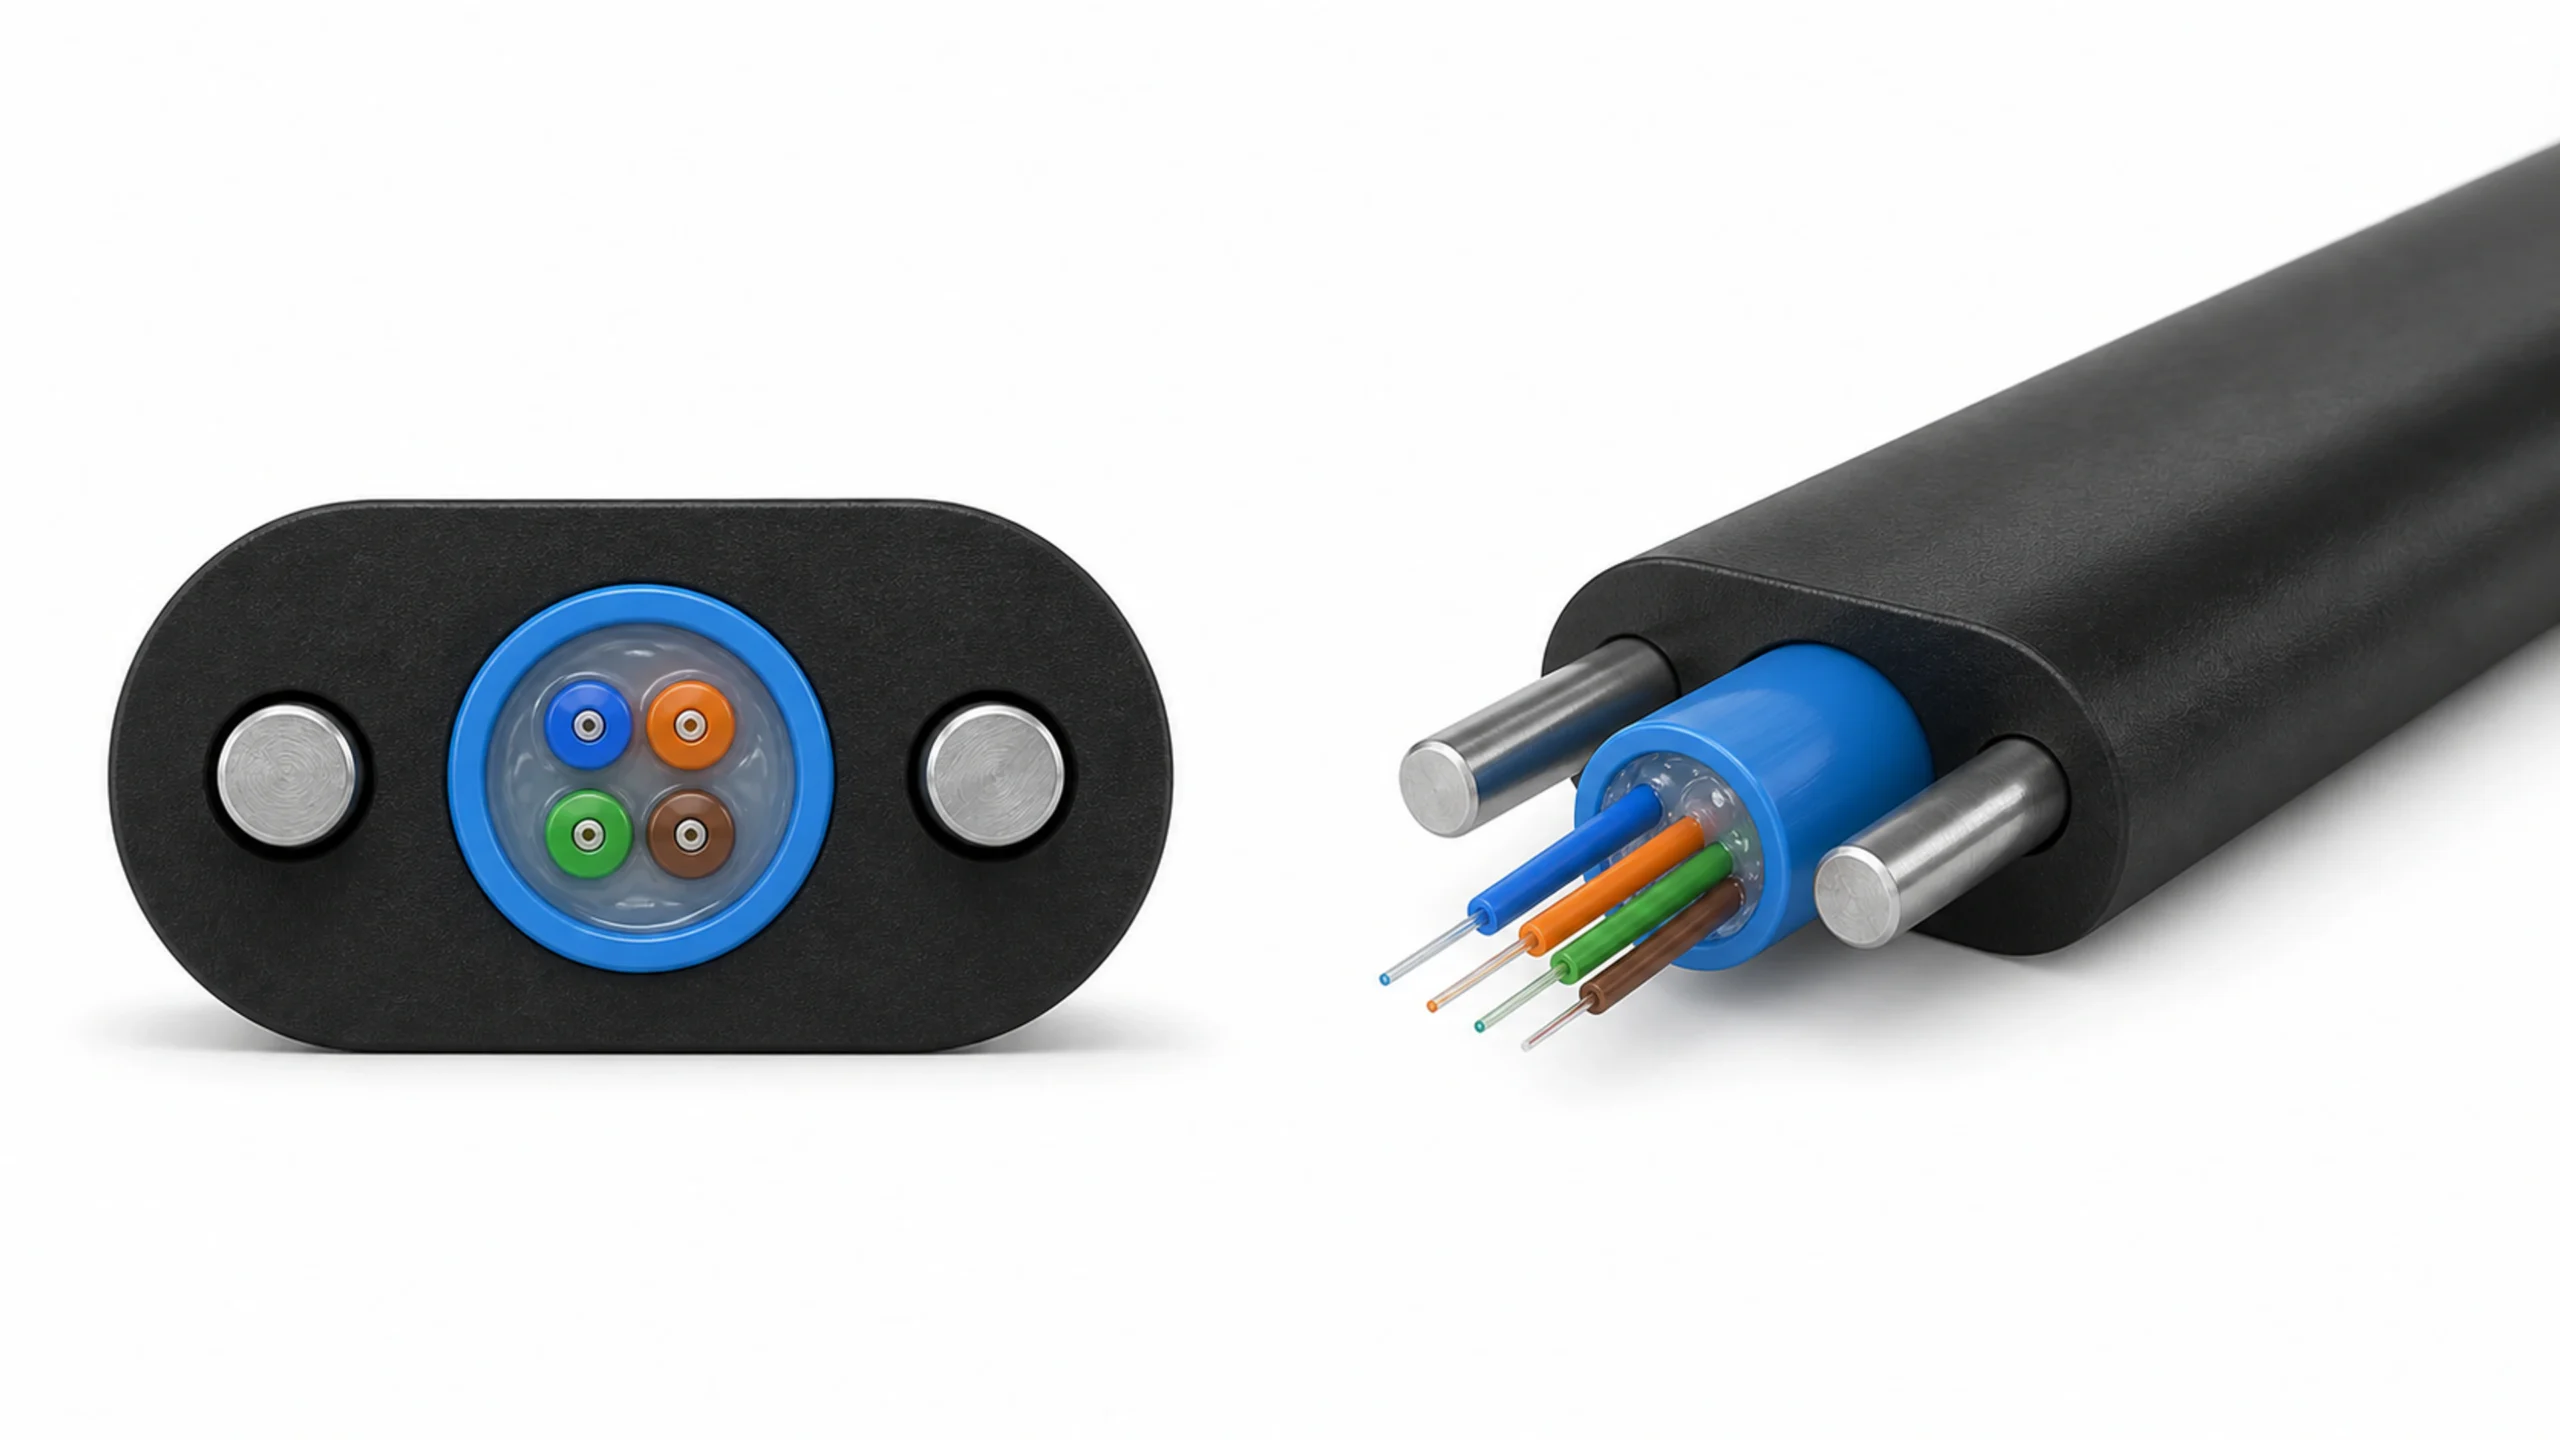
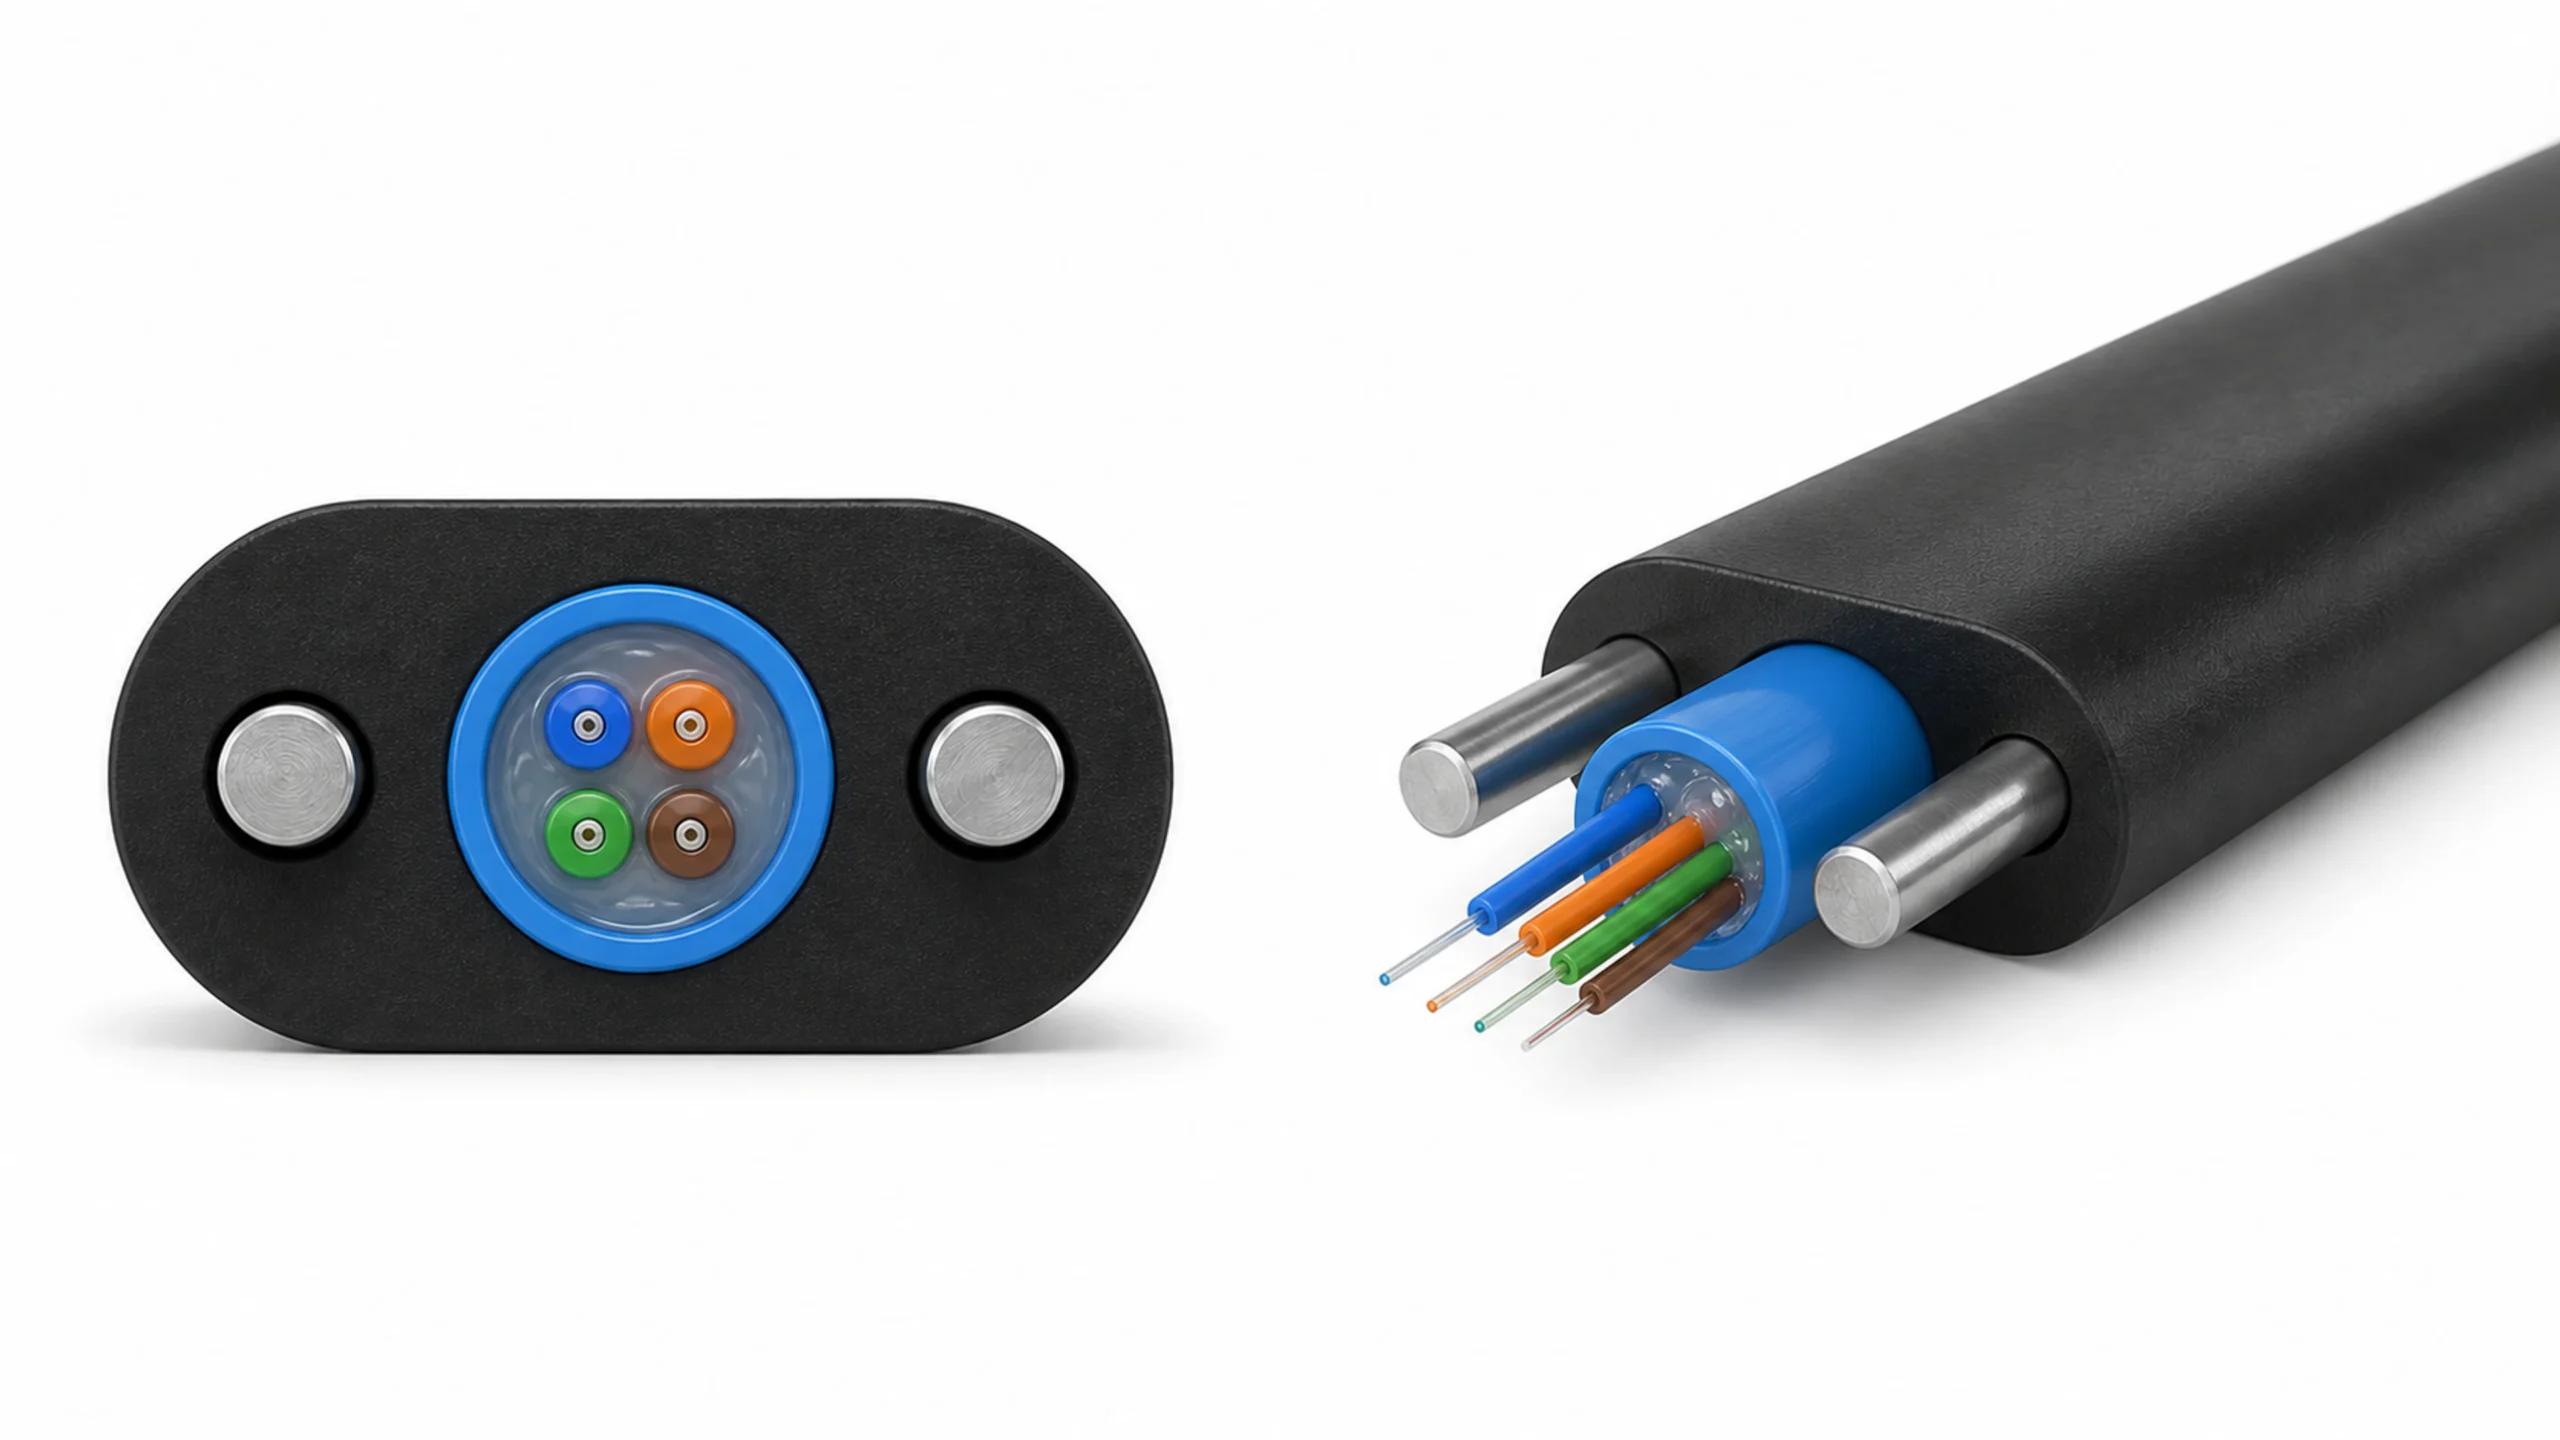
Construction matters: armored, all-dielectric and figure-8 cables require different preparation, reinforcement and tooling. One illustrated arrangement does not establish compatibility with every cable.
See the sheathing process. Plan the acceptance trial.
The HONGKAI HK-90 video shows a sheathing reference for an ADSS cable route. Use it to discuss equipment and operating sequence, then agree the trial for your construction.
01PRODUCT
Trial the specified construction.
Use the approved core, sheath compound, protection materials and output drum.
02PROCESS
Check coordinated behavior.
Observe extrusion, cooling, diameter monitoring, traction and take-up during starts, steady running and stops.
03OUTPUT
Agree the inspection record.
Check finished diameter, sheath thickness and appearance, marking, winding and the agreed optical and jacket tests.
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
01
Оборудование
Specify the supplied modules and quantities
Identify retained and buyer-supplied equipment
Record equipment-source responsibilities
02
Line integration
Review layout and material-flow interfaces
Define controls, utilities and safety boundaries
Согласовать объем работ по монтажу и пусконаладке
03
Start-up & support
Define trial products and acceptance records
Confirm operator training and documentation
Agree spare-parts and after-sales scope
09START THE ENGINEERING REVIEW
Tell us about the cable you need to sheath.
Start with your drawing, product requirements or existing equipment. Technical details can be confirmed during the first review.
WHAT TO PREPARE
Nine inputs for your sheathing line.
01
Cable drawing and finished dimensions
02
Incoming core or loose-tube details
03
Sheath compound and jacket thickness
04
Reinforcement, tape and ripcord requirements
05
Input and output drum sizes / weights
06
Target output and operating plan
07
Marking, testing and acceptance criteria
08
Factory layout and retained equipment
09
Utilities, installation and project timing
10BUYER FAQ
Questions before specifying an HK-90 sheathing line.
Review the cable construction, equipment boundary and information needed for a proposal.
01Что производит оболочечная линия HK-90?
It applies the specified outer sheath to a prepared optical cable core or construction-specific tube and protection package, then cools, inspects and collects the cable. Upstream fiber coloring, loose-tube extrusion and SZ stranding are separate stages unless included in the project scope.
02Может ли одна линия выпускать кабели GYXTW, ADSS и кабели с фигурным 8?
Эти семейства кабелей могут включать этап оболочки HK-90, однако они не используют один и тот же комплект оборудования. Обработка сердечника, армирование, бронирование, позиционирование несущего элемента, оснастка крестовины и последующие испытания должны быть пересмотрены для каждого чертежа кабеля.
03Включает ли каждая конфигурация оборудование для металлической ленты?
Нет. Выбраны размотка металлической ленты, соединение, накопление, гофрирование и продольная формовка для указанной бронированной или композитной оболочки. Маршрут с полностью диэлектрической конструкцией предъявляет иные требования к армированию.
04Что означают указанная скорость и выходной сигнал?
The source gives up to 80 m/min for PE cable below 10 mm and an extrusion-output reference of up to 250 kg/h PE with the crosshead open. These values describe stated reference conditions. Actual accepted cable output must be agreed for the cable, compound, tooling, cooling and operating plan.
05Какие составы оболочек можно использовать?
The supplied extruder reference describes PE and PVC. Confirm the exact grade and required screw, tooling, drying and temperature settings. Do not assume that LSZH or another compound is covered without a separate engineering review.
06Входит ли в комплект аккумулятор готового кабеля?
Ссылка на оборудование включает аккумулятор металлической ленты, который хранит ленту для её последовательного соединения. Аккумулятор готового кабеля выполняет другую функцию и требует собственной конфигурации, натяжения, длины хранения и проверки при замене катушки.
07Можно ли использовать испытательную установку для оболочки с искровым разрядом для ADSS?
Применимость испытания зависит от конструкции кабеля и наличия подходящего электрического обратного пути. Диэлектрический кабель не должен автоматически получать ту же схему испытания высоким напряжением, что и кабель, содержащий металл. Подтвердите метод испытания и критерии приемки для конкретного изделия.
08Что мне нужно отправить для получения коммерческого предложения?
Отправьте чертеж кабеля, входящую жилу, компаунд оболочки, материалы защиты, требуемые размеры барабанов и производственную цель. Приложите планировку вашего завода и имеющееся оборудование, если это возможно. Технические детали можно уточнить во время первого обзора.
We've detected you might be speaking a different language. Do you want to change to:





 English
 हिन्दी
 فارسی