






A factory may receive an enquiry for “22 AWG wire” and still lack the information needed to select its cable machinery. The gauge does not say whether the factory will buy a finished conductor, draw individual wires, assemble strands or apply insulation.
Use AWG as one field in the conductor specification, not as a substitute for material, strand construction, actual dimensions, reel drawings or acceptance requirements. Each production stage needs the dimensions of the material that actually enters and leaves it.
This guide is for factory owners, production managers and technical buyers preparing machinery enquiries. It does not select a conductor for an electrical installation or provide current-carrying, circuit-protection or installation-code advice.
Why the Same AWG Can Mean Different Outside Diameters
AWG means American Wire Gauge. ASTM B258 defines nominal diameters and cross-sectional areas for AWG sizes of solid round wire. Its scope is not a finished-cable diameter table.1 “스트랜디드(stranded)”라는 단어를 추가하는 것 역시 와이어의 고유한 배열을 정의하지 않는다.
A complete product model tied to an identified specification may already provide the construction and dimensions needed for an enquiry. In that case, send the specification and its revision with the model. An AWG number by itself is only the gauge designation; it does not identify the conductor metal, coating, strand arrangement or finished-wire diameter.
Keep material and construction as separate decisions. Copper or tinned copper describes material or coating; solid or stranded describes how the conductor is built. The customer’s required product determines these choices. Whether the factory buys that conductor or makes it in-house is a further decision about the machinery scope, not a property of the AWG number.
게이지 옆의 구조를 읽으십시오. 다음과 같은 지정은 22 AWG, 7/30 identifies a 22 AWG conductor made from seven 30 AWG wires. The “30” is the individual wire’s gauge, not a diameter in millimetres. For a solid conductor there is only one wire, so the individual-wire diameter and the uninsulated conductor diameter refer to the same physical object.

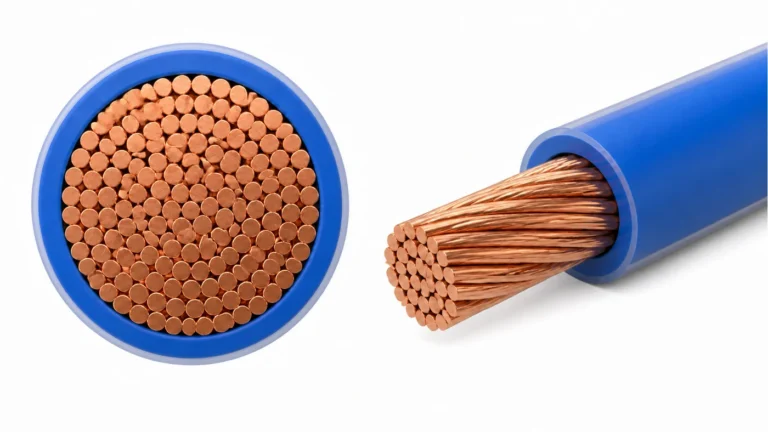
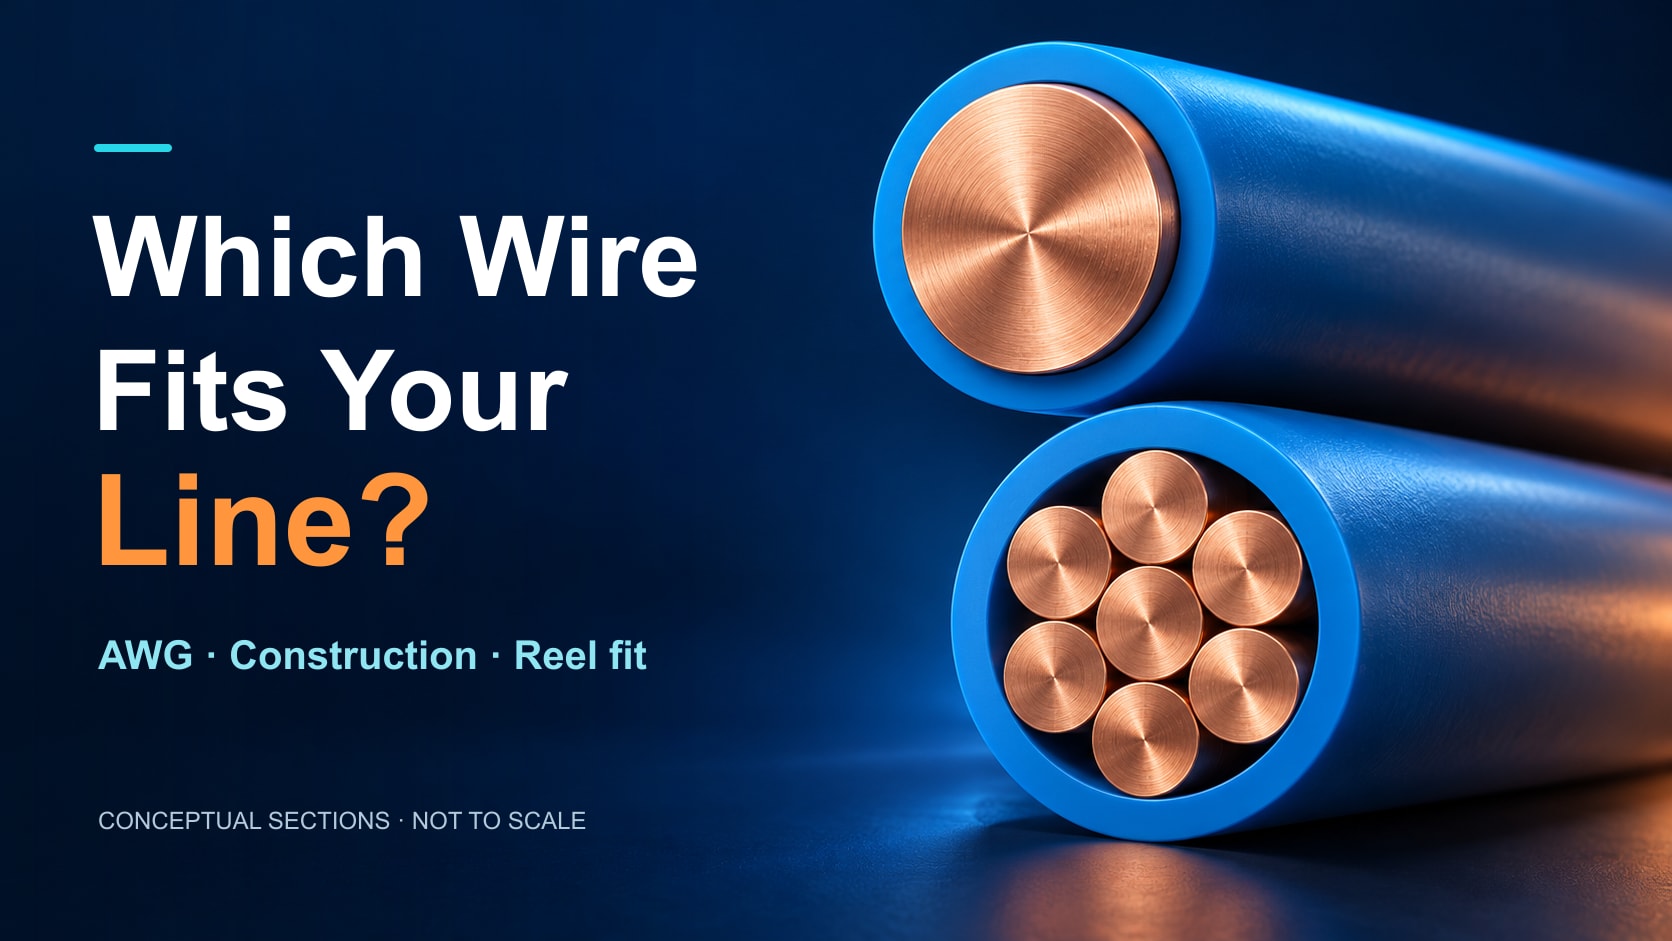
도체 구조 및 외부 피복의 개념적 비교. 출시된 제품의 치수는 표에 유지되며, 도면은 제조 도면이 아닙니다.
Published products make the distinction concrete. Alpha Wire lists the following two tinned-copper hook-up wires under the same 22 AWG designation.23
| Published product | 도체 구조 | 표시된 도체 직경 | 표면 PVC 벽 | Listed insulated-wire diameter |
|---|---|---|---|---|
| Alpha Wire 3051/1 | Solid, 22 AWG | 0.025 in | 0.016 in | 0.057 ± 0.002 in |
| Alpha Wire 3051 | Seven wires, 22 AWG (7/30) | 0.030 in | 0.016 in | 0.062 ± 0.002 in |
These are the manufacturer’s stated values for those particular products, retained in their published units. They are not universal dimensions or tolerances for all 22 AWG conductors, and they are not HONGKAI production results. The useful comparison is that the gauge and nominal insulation wall are the same while both the conductor diameter and the insulated-wire diameter differ.
For equipment selection, keep three quantities separate:
- Metal cross-sectional area: the area of the conducting material, expressed in a specified unit such as square millimetres.
- Conductor outside diameter: the outside envelope of the uninsulated solid or stranded conductor.
- Insulated-wire outside diameter: the envelope after the specified insulation has been applied.
The spaces between round strands explain why a stranded conductor’s outside envelope cannot be treated as a solid metal circle. For an ideal set of equal round wires, the sum of the individual wire areas is n × π × d² / 4, where n is the wire count and d is the individual-wire diameter. This is a geometric sum, not a rule for assigning an AWG size or a finished-conductor acceptance method. The conductor’s actual arrangement, lay, coating and any compaction still need to be specified.
Note: Do not relabel a rounded AWG-to-mm² comparison as an approved metric conductor specification. Keep the original designation, governing specification and controlling dimensional units visible; an engineering comparison is not permission to substitute another product.
Give Each Machine the Dimensions It Actually Uses
A supplier cannot select a complete production route from the final AWG number alone. First decide which material the factory purchases and which transformation the proposed equipment must perform.
If the factory buys a conductor ready for insulation, conductor drawing and assembly may be outside the purchase. If it buys individual wires, the required conductor construction determines the assembly stage. If it starts with larger wire or rod, the drawing route needs its own input and output definition. These are alternative scope boundaries, not a recommendation that every factory should own every operation.
In HONGKAI’s enquiry assessment, the first distinction is therefore between buying ready-made conductors and purchasing equipment to make them. A broader mix of wire sizes can be a reason to evaluate in-house drawing, while limited demand or a small product range may make that investment difficult to justify. Neither condition establishes savings on its own: compare the actual product mix, required volume, available feedstock and quoted purchase and operating costs before adding a drawing machine.

Conceptual material handovers for drawing, conductor assembly and insulation. The purchased scope determines which stages are required; these are alternative starting points, not a requirement to own every operation.
| Operation under review | Product data to provide | What the offer needs to resolve |
|---|---|---|
| Individual-wire drawing | Feed material and condition, starting diameter, required individual-wire diameter and tolerance, required final condition | The reduction and finishing scope, including whether annealing is part of the offer |
| Bunching or stranding | Number and size of individual wires, material and coating, required construction, lay requirements and finished conductor envelope | 제안된 조립 방식이 지정된 입력값으로 해당 구조를 구현할 수 있는지 여부 |
| 절연 사출 | Actual incoming conductor size range and surface condition, insulation compound, required wall and finished-wire dimensions | Material-processing scope, guide and tooling review, centring checks and the proposed trial product |
| Pay-off and take-up | The package entering and leaving each stage, dimensioned reel drawing, empty and loaded mass, winding and handling requirements | Physical fit, support and drive arrangement, controllable handling and transfer to the next stage |
For drawing, do not send only the area of the assembled conductor. A drawing proposal needs the individual wire that must be produced. For assembly, keep individual-wire diameter, wire count and finished conductor diameter together in the same specification. This three-part check makes the intended input and output explicit; the supplier must still confirm the required construction and assembly method, not simply match one outside diameter in a catalogue.
Bunching and ordered stranding should not be treated as interchangeable catalogue names. For example, ASTM B8’s public scope describes concentric-lay conductors with a centre surrounded by helically laid layers.4 Whether that specification applies is a product-design decision; its construction cannot be replaced by an unspecified bunch merely because the nominal size is similar.
An extrusion enquiry then needs the conductor that will actually pass through the crosshead. Identify whether its stated diameter is a design target, a measured value or a permitted range. Keep the insulation compound and wall requirements in separate fields rather than deriving them from AWG.
HONGKAI’s bunching equipment selection page separates individual-wire details, finished-conductor construction, lay and output-package requirements. Those are distinct selection inputs, not one interchangeable “wire size”. The page is a family-selection reference, not a project-specific operating-range table; the selected construction and the offered machine still require confirmation. No model range, speed or delivery experience is assumed in this guide.
The result of this step should be a stage-by-stage input record. Where a value is not known, mark it as unresolved in the enquiry instead of allowing a supplier to fill it with an unacknowledged assumption.
Keep the Specification Attached to the Reel and the Test Result
Dimensions describe the product, but a useful equipment enquiry also identifies how that product will arrive, be handled and be checked. A conductor sample without a drawing revision or reel identity is difficult to connect to a later machine trial.
Reel Geometry Is a Separate Input
Identify whether the customer will use steel reels, wooden drums or another agreed package; do not leave the material and construction implicit. Provide the reel’s flange diameter, barrel diameter, usable winding width, overall width and bore or mounting details. Also state the empty mass, maximum intended loaded mass and the proposed loading method. A single nominal reel-size label does not communicate all of these features.
Compare the same drawing at the upstream take-up and downstream pay-off. Ask the supplier to identify any required adapter, transfer or rewinding stage explicitly. Do not assume that a reel can be reused merely because its flange diameter fits both machines.
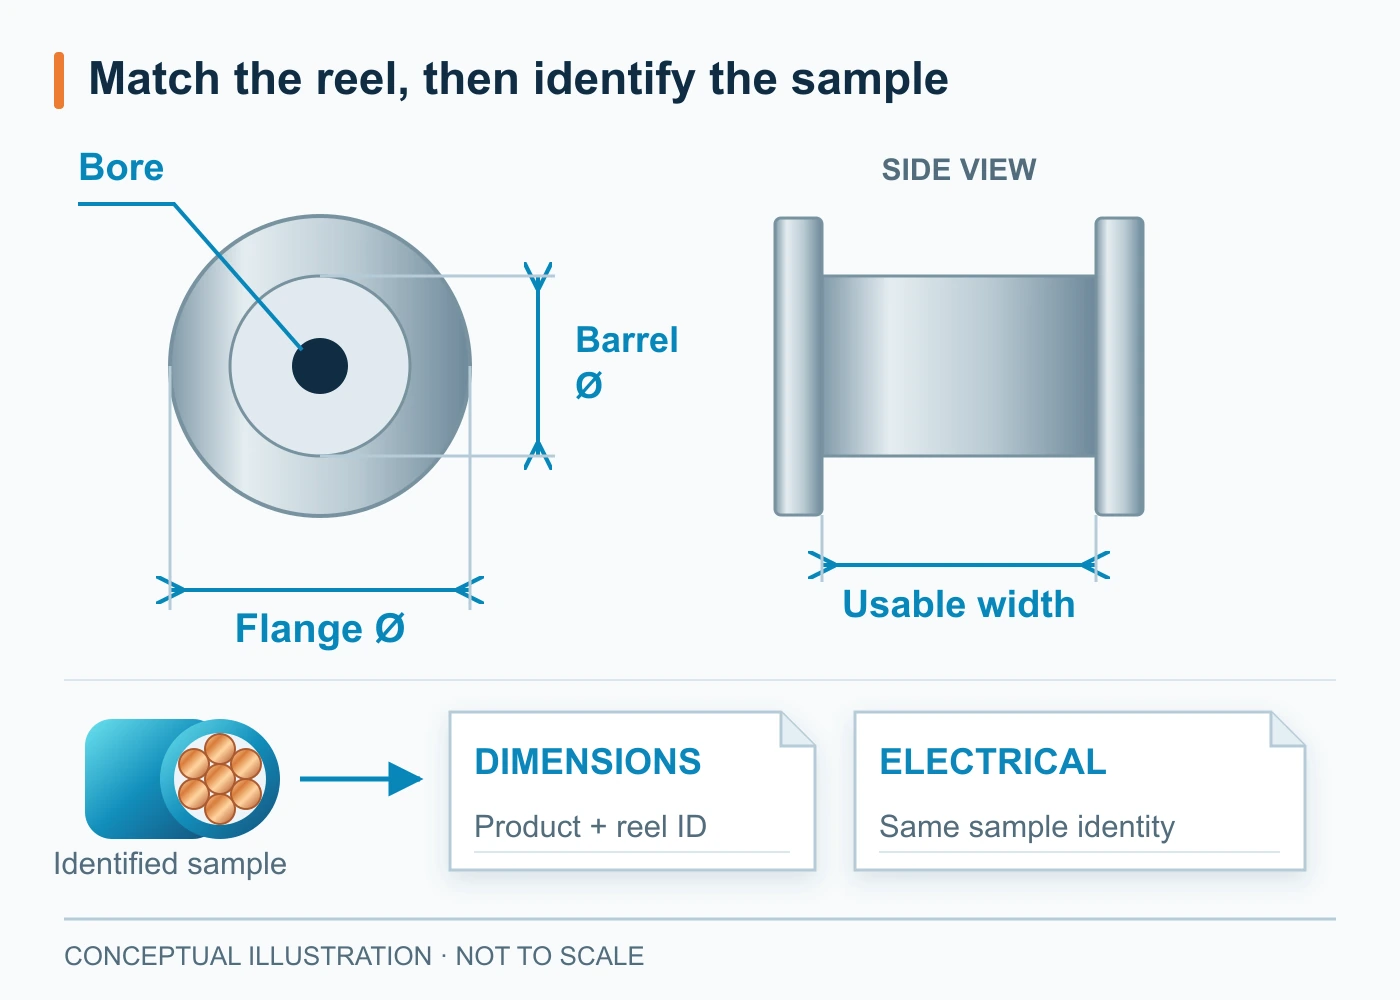
Illustrative package-interface and sample-record relationship. Reel dimensions, loading arrangements, dimensional checks and electrical test responsibilities must be agreed for the selected product.
For a trial, retain the package identification with the conductor construction and the winding requirements. Where handling stability matters, define the package conditions that must be demonstrated rather than approving the arrangement from an unloaded reel alone. These are proposed purchase checks, not a universal test sequence or an equipment-load rating.
Manufacturing Checks and Electrical Tests Need Separate Evidence
For a conductor-assembly trial, identify the incoming individual-wire size, wire count and required assembled diameter. For the specified insulation or sheathing operation, identify the incoming conductor and the required finished dimensions. The purchase specification should say which dimensions are measured, how they are measured and which product-specific limits govern acceptance.
These manufacturing checks are not substitutes for the finished wire’s electrical tests. Define who supplies the additional instruments, performs each test and issues the result. If test equipment or testing services are included in the machinery contract, list them explicitly; otherwise, make the customer’s separate testing arrangements visible. Separating the evidence does not remove either party’s agreed responsibilities.
An outside-diameter check does not measure electrical resistance. ASTM B193’s public description treats specimen dimensions, resistance measurement and correction to a reference temperature as parts of determining conductor-material resistivity.5 That does not make B193 the automatic release standard for every finished wire.
For the selected product, ask the responsible engineer to identify the applicable resistance requirement and test method. The resulting record should connect the sample identity, measured length, test temperature, instrument and method to the reported result. If a correction is used, retain its basis. State whether the reported number is an actual measurement, a normalized result or a catalogue nominal value.
Keep dimensional and electrical evidence distinct. The manufacturer’s data for a particular construction can help define an enquiry, but copying a catalogue value into a trial record does not demonstrate that the trial conductor met it. Likewise, a successful resistance result does not by itself prove the strand count, insulation wall or reel interface.
Evidence to request: One identified conductor specification, its material and construction record, the relevant dimensional measurements, the agreed electrical or mechanical test results, and the reel drawing used for the trial. Each acceptance limit must point to the approved product requirement, not a generic AWG chart.
Build a Conductor Record That Two Suppliers Can Quote Consistently
The final purchasing document should make it difficult for two suppliers to interpret the same gauge differently. HONGKAI’s practical starting point is a clearly identified product and a stated production requirement; the same definition should carry through the equipment configuration and contract to the acceptance criteria. Organize it around one conductor construction at a time, with the following linked records:
- Product identity: the cable or wire application, drawing number and revision, conductor designation and governing specification.
- Material and construction: metal, coating and condition; solid or stranded; individual-wire count and size; assembly method and lay where required.
- Stage dimensions: the actual input and output dimension at every purchased operation, with units, limits and measurement basis.
- Package interfaces: incoming and outgoing reel drawings, mass limits and transfer or loading arrangements.
- Output and demonstration basis: the required production output, its units and associated product; materials and reels for the trial; measurements, acceptance criteria and responsibilities.
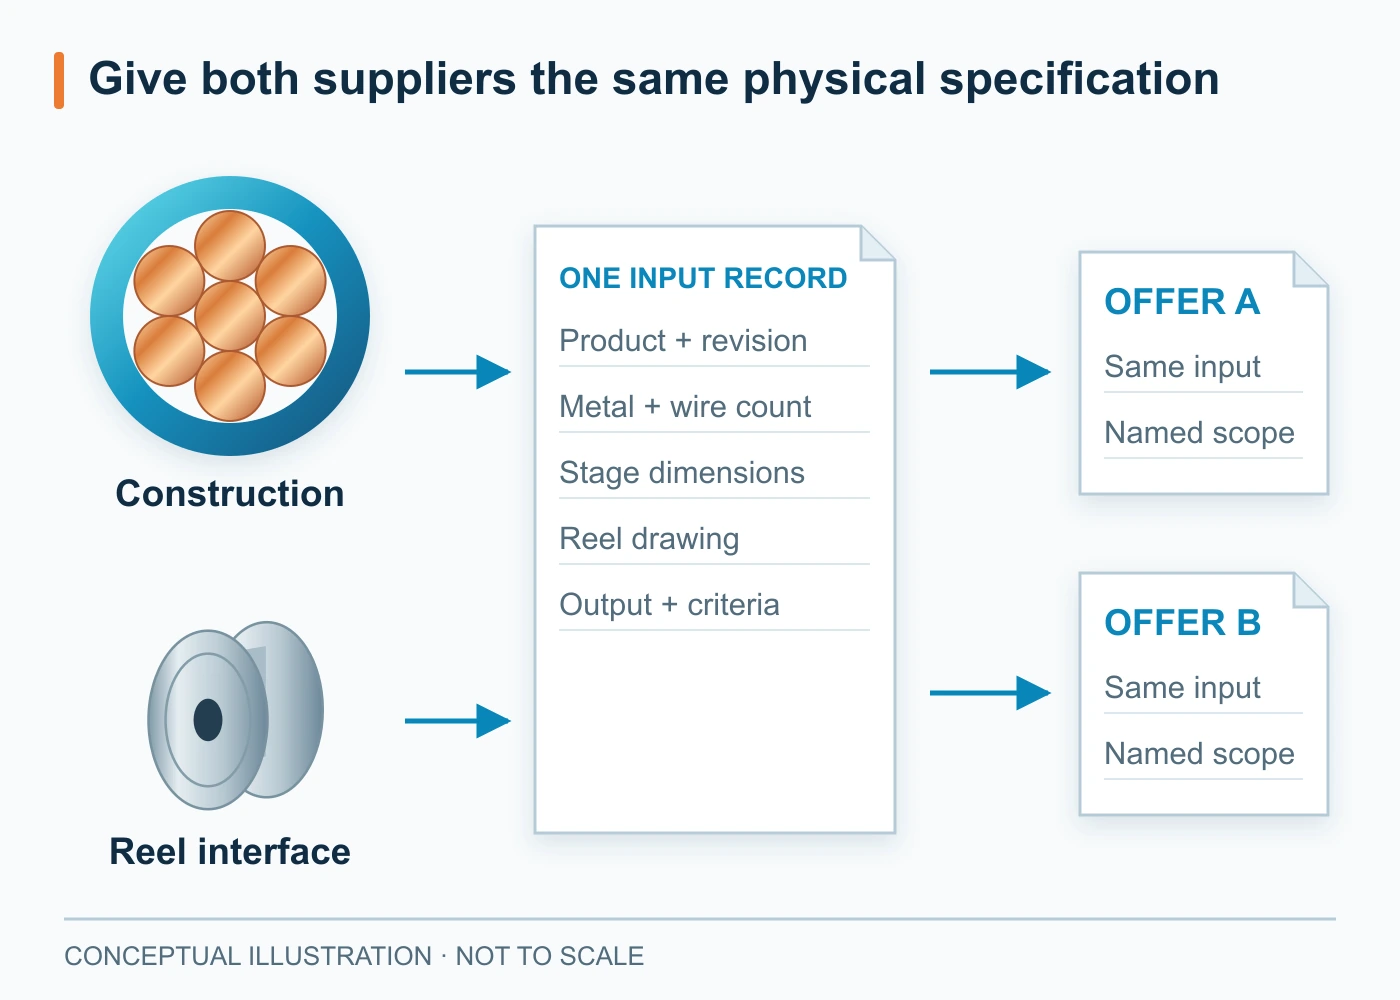
Conceptual quotation comparison: both offers must refer to the same conductor construction, dimensions and package interfaces. The blank records are not actual quotations or acceptance results.
“22 AWG machine” leaves all five records open. “Insulation extrusion for an identified, purchased 22 AWG conductor” at least defines the operation and starting point, but still needs the conductor envelope, compound, wall, finished dimensions and packages before it becomes a complete specification.
If an alternative construction is acceptable, give it a separate record. Do not let a different strand count or conductor material disappear into a general statement that both products have the same AWG. Ask the supplier to identify which tooling, handling conditions or trials change with the alternative.
When comparing quotations, trace each offered machine back to the operation it owns and the conductor record it accepts. Separate the factory’s current products from future options. A demonstrated operating condition for one conductor is not evidence of performance across an unspecified gauge range.
Keep the product drawing, configuration sheet and contract consistent when the required construction or output changes. Name the trial product and conditions beside the output requirement, and attach the agreed acceptance criteria. A target in an enquiry is not an independently demonstrated result until the agreed trial and measurements support it.
The practical output is not a larger conversion chart. It is an agreed description of the metal, the construction, the physical envelope and the package at each handover. Once those inputs are fixed, machine selection and acceptance discussions can refer to the same product.
-
ASTM B258-18(2026), official scope and edition record. The public record concerns nominal AWG dimensions for solid round wires; it is not a finished-cable specification. This guide does not reproduce the standard’s dimensional tables. ↩
-
Alpha Wire 3051/1, product construction. Product-specific solid-conductor, wall and insulated-wire dimensions, checked on 29 October 2026. ↩
-
Alpha Wire 3051, product construction. Product-specific seven-wire, wall and insulated-wire dimensions, checked on 29 October 2026. These two examples illustrate specification differences, not a recommendation to copy either product. ↩
-
ASTM B8-23, official scope. The public description distinguishes concentric-lay construction; applicability and detailed requirements must be selected for the intended product. ↩
-
ASTM B193-25, official method overview. The public description identifies dimensional and resistance measurements and temperature correction. It is not a substitute for the applicable full method or the finished product’s acceptance requirements. ↩
 English
 हिन्दी
 فارسی