


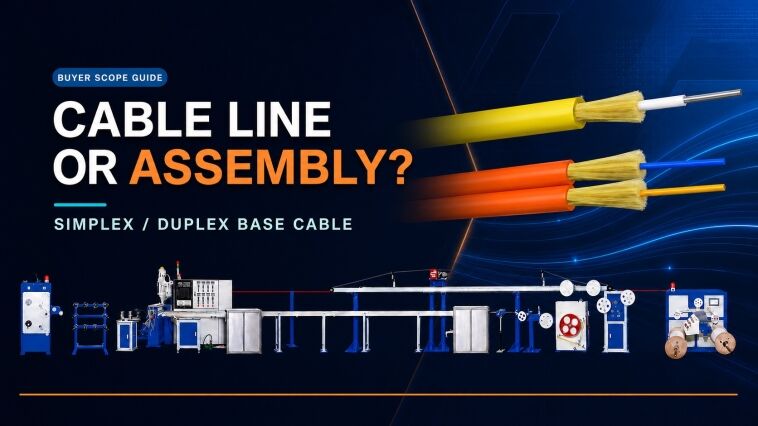
A fiber optic cable factory owner, production manager or technical buyer planning conventional patch cords must define two connected scopes. One scope makes the simplex or duplex base cable; the other cuts that cable and turns each end into an inspected, optically tested connector assembly.
A complete fiber optic patch-cord factory is not one extrusion line. It is either a qualified purchased-cable supply plus a complete connector-assembly workcell, or an integrated route that adds tight-buffer and outer-jacket production before the same back-end workcell.

نقشه دامنه خریدار: خط تولید کابل، کابل پایه سیمپلکس یا دوپلکس تولید میکند؛ و سلول کاری جداگانهی مونتاژ کانکتور، آن کابل را به یک کابل پچ LC یا SC نهایی تبدیل میکند.
This guide maps the complete manufacturing boundary for conventional LC and SC patch cords. FC and ST may be added as project-specific fixture variants, but they are not the main production scope in this article. MPO and MTP multi-fiber assemblies are excluded because their cable construction, ferrule preparation, polishing, geometry control, polarity and multi-channel testing require a separate project scope.
یک کارخانه کامل کابل پچ شامل چه چیزهایی میشود؟
A complete patch-cord route must end with a saleable, traceable connectorized product—not merely a reel of cable or a visually polished connector. The proposal needs an owner and acceptance record for every stage from incoming fiber or cable through final optical test and packing.
| Manufacturing boundary | ورودی | خروجی اصلی | مدارک قبل از انتشار |
|---|---|---|---|
| تولید بافر فشرده هنگامی که کابل پایه در داخل شرکت ساخته میشود | ترکیب فیبر نوری و بافر تأییدشده | فیبر با روکش محکم واجد شرایط | هویت مادی، ابعاد، وضعیت سطح و بازرسی نوری توافقشده |
| تولید آرامید و روکش بیرونی هنگامی که کابل پایه در داخل شرکت ساخته میشود | ترکیب فیبر با بافر فشرده، آرامید و روکش تأییدشده | کابل سیمپلکس یا دوپلکس روی یک ردیف | کشش کابل، ابعاد، شناسه سیمپیچ، ظاهر و بازرسی نوری توافقشده |
| Cable preparation | رول رهاشده یا کابل واجد شرایط خریداریشده | سرهای کابل برشخورده و آمادهشده | طول، جهتگیری، ابعاد نوار و هویت مسافر |
| Connector assembly | کابل آمادهشده، قطعات کانکتور و مصرفیهای تأییدشده | انتهای کانکتور مونتاژشده و ولکانیزهشده | شمارهٔ لات قطعه، تنظیمات فرآیند و سوابق دسته یا اپراتور |
| بازرسی سطح صافشده و انتهای سیم | مجموعه اتصالدهنده پایدارشده | تمیز کردن سطح انتهایی فِرول | فرآیند پولیش تأییدشده و نتیجه بازرسی ذخیرهشده یا قابل ردیابی |
| آزمایش و پرداخت نوری | کابل پچ کاملشده | محصول قابل فروش آزاد شده | تنظیمات آزمایش، طول موج، نتایج، هویت، برچسب و سوابق بستهبندی |
The خط تولید کابل پچ کورد HONGKAI supports the base-cable side for applicable constructions. The confirmed project route then adds partner-integrated back-end stations, together with connector-specific fixtures, hand tools and consumables. HONGKAI’s published مدل تولید و ادغام تخصصی explains this source boundary; the final commercial proposal must still distinguish HONGKAI-manufactured equipment, partner-integrated equipment and buyer-supplied items.
Common mistakes: A quotation calls the cable line a complete patch-cord factory but omits connectorization and optical testing. Another quotation lists a polishing machine but omits its connector fixtures, films, inspection adapter, reference cords or process responsibility.
کدام خطوط HONGKAI کابل پایه را تشکیل میدهند؟
For the reviewed simplex or duplex construction, the HONGKAI route uses the HK-30 to produce tight-buffered fiber and the HK-50 to apply aramid reinforcement and the outer jacket. If the factory purchases qualified tight-buffered fiber, the cable-making scope can start with the HK-50.
HK-30 tight-buffer stage
The reviewed HK-30 configuration receives optical fiber and applies the specified tight-buffer layer. Its functional modules include controlled payoff, preheating, material drying and feeding, extrusion, warm and cold cooling, online diameter measurement, capstan control and take-up. These functions define the production stage; the customer’s approved construction must define the actual polymer, color, dimensions, reel format and acceptance limits.
Verified HONGKAI HK-30 3D reference showing the complete tight-buffer production line. Final tooling, material and operating values remain project-specific.
HK-50 aramid-and-jacket stage
The reviewed HK-50 configuration receives the approved tight-buffered input, pays off the aramid reinforcement and extrudes the outer jacket. Its functional modules include input payoff, adjustable aramid payoff, positioning, material preparation, extrusion, cooling, online diameter measurement, capstan, accumulation and take-up.

Verified HONGKAI HK-50 3D reference showing the complete line used for an applicable aramid-reinforced simplex or duplex jacket stage. The accepted cable construction controls the final configuration.
The complete in-house route is therefore HK-30 tight buffering followed by HK-50 aramid reinforcement and jacketing. An HK-50-only route is appropriate when the factory has an approved external source for tight-buffered fiber and the incoming package, material, dimensions and optical condition match the signed HK-50 input specification.
The HK-30 and HK-50 documents are older project configurations. They verify the process stages and equipment functions, but their speeds, tensions, power, output, material options and package sizes must not be copied into a new proposal without reconfirmation.
The earlier HONGKAI راهنمای فرآیند کابل پچکورد also shows the HK-30 and HK-50 as separate production stages. Use it as orientation only; the approved cable drawing and current technical agreement control a new project.
How to verify: During FAT, connect the raw-fiber or tight-buffer input to the approved recipe and identify the resulting reel. Retain the actual cable drawing, material lots, tooling, dimensions, surface result, optical check and take-up package used for the trial.
فرآیند کامل پشتسری یک کابل رشتهای LC یا SC چیست؟
The supplied conventional LC/SC package covers cable cutting, jacket and buffer stripping, adhesive preparation and dispensing, connector assembly, crimping, curing, fiber scribing, polishing, end-face inspection, optical testing, labeling and packing. The ten powered back-end stations are integrated through HONGKAI’s specialist partner; connector-specific hand tools, fixtures and consumables complete the route.
The sequence below is a controlled planning route for the supplied epoxy-and-polish package. It is not a universal connector recipe. The approved connector-component instructions must set the exact strip dimensions, cleaning method, adhesive, assembly order, crimp tooling, cure cycle, polish sequence and optical limits. A factory should turn those instructions into a traveler or batch record before FAT.
1. Release the incoming cable and production order
Before cutting, verify the cable drawing, connector family, ferrule finish, finished length, quantity, label data and test requirements. Record the incoming reel or cable lot against the work order. If base cable is made in house, the released HK-50 reel is the handoff point; if it is purchased, the supplier’s reel identity and incoming inspection are the handoff evidence.
نحوه تأیید: اپراتور باید بتواند هر نمونه FAT را به یک ردیف کابل تأییدشده، یک لات قطعه کانکتور و یک نسخه دستورالعمل کاری مرتبط کند.
2. Cut the cable to controlled length
The automatic fiber cable cutting machine measures and cuts the released cable for the planned patch-cord length. The RFQ should define the cable-size range, required length range, tolerance, quantity count and whether allowance for stripping and connector assembly is included in the cutting instruction.
3D technical model based on the verified automatic cable cutting machine in Peter’s supplied conventional patch-cord package. Supplier branding has been removed; this back-end station is integrated through HONGKAI’s specialist partner.
اشتباه رایج: فقط طول برش نمایشدادهشده را قبول نکنید. در طی تست پذیرش کارخانه (FAT)، یک نمونه مشخص را اندازهگیری کرده و هم مقدار تنظیمشده و هم نتایج واقعی را نگهداری نمایید.
3. Strip the outer jacket
The optical cable stripping machine removes the required jacket length so the aramid yarn and buffered fiber can be prepared for the connector. The work instruction must match the actual simplex or duplex cable diameter, jacket material and connector boot or crimp sleeve. Acceptance should cover strip length, a clean cut and no damage to the reinforcement or buffered fiber.
3D technical model based on the verified outer-jacket stripping station. Supplier branding has been removed; final tooling is selected against the approved cable and connector construction.
4. روکش محافظ داخلی را جدا کنید
The buffer stripping machine exposes the glass fiber to the dimension required by the connector assembly process. The operator must control the strip length and inspect the exposed fiber for coating residue, scratches or breakage. The machine does not replace cleaning and handling discipline.
3D technical model based on the verified tight-buffer stripping station in the supplied LC/SC package. Supplier branding has been removed.
چه چیزی بپرسیم: محدوده قابل قبول کابل و بافر، لیست تیغها یا ابزارهای جایگزین، روش تأیید طول پوستهکنی و معیارهای رد فیبر آسیبدیده را درخواست کنید.
5. Prepare adhesive with the Model 800 centrifuge
For the reviewed epoxy-and-polish route, the approved adhesive is prepared according to its supplier instruction. The Model 800 epoxy centrifuge supports controlled preparation and removal of entrained air before dispensing. Adhesive identity, mix ratio when applicable, preparation time, usable life, storage condition and disposal rule belong in the batch record.
3D technical model based on the verified epoxy centrifuge in the supplied package. Supplier markings have been removed; the approved connector and adhesive suppliers—not the image—define the preparation recipe.
چالش: یک فهرست ماشینآلات که تنها عبارت “اپوکسی” را ذکر میکند، خریدار را بدون سیستم چسب سازگار، کنترل دستهای یا قاعدهای برای عمر قابل استفاده رها میکند.
6. چسب را توزیع کنید
The epoxy dispenser delivers the prepared adhesive to the connector assembly process. The dispensing needle or adapter, dose, cleaning interval and confirmation method must suit the selected LC or SC connector components. Record the adhesive batch and preparation time with the work order.
3D technical model based on the verified adhesive dispensing station in the supplied conventional connector route. Supplier branding has been removed.
7. Insert the fiber, assemble components and crimp
The operator threads the prepared fiber into the ferrule, seats the cable and assembles the boot, crimp sleeve and other specified parts in the connector supplier’s approved order. The pneumatic crimping machine applies the connector-specific crimp through the correct die or fixture. The factory must provide stable compressed air at the agreed pressure and quality.
3D technical model based on the verified pneumatic crimping machine. Supplier branding has been removed; the connector construction controls the die, crimp position and acceptance check.
How to verify: Inspect component seating, aramid capture, boot position and crimp condition on representative LC and SC assemblies. Record the die or fixture identity and compressed-air condition used for FAT.
8. Cure the connector assembly
The curing oven stabilizes the adhesive under the approved time-and-temperature instruction. The work instruction must define loading orientation, fixture or holder, setpoint, actual cycle evidence, batch size and handling after cure. Do not transfer a cure recipe from another adhesive or connector system without approval.
3D technical model based on the verified connector curing unit in the supplied LC/SC package. Supplier branding has been removed.
مدارک درخواستی: یک بازرس FAT باید هر نمونه را به لاتکس چسب، شناسه کوره، سوابق چرخه و اپراتور مسئول مرتبط کند.
9. Scribe excess fiber and prepare the ferrule for polishing
After the approved cure and cooling sequence, use the specified fiber cutting pen or scribing tool to remove the protruding fiber without chipping the ferrule or damaging the fiber. Clean the connector and polishing fixture before loading. This is a hand-tool step in the supplied package, not a reason to invent another machine.
اشتباهات رایج: اعمال نیروی بیش از حد هنگام خراشدادن، ورود ذرات معلق به فیکسچر پولیش و عدم وجود قاعدهای برای تعویض ابزارهای دستی ساییدهشده.
10. فرولهای LC و SC را پولیش کنید
The fiber connector polishing machine performs the mechanical polishing stage. A complete station also needs the correct LC or SC holder, the approved UPC or APC process where applicable, polishing pads and films, cleaning materials and a controlled film-change rule. Peter’s supplied package lists connector-specific fixtures; they must be scheduled by actual launch product rather than assumed from the machine name.
3D technical model based on the verified polishing machine in the supplied package. Supplier branding has been removed; LC and SC require the correct connector-specific holder and approved consumable sequence.
چه چیزی بپرسید: درخواست یک ماتریس اتصالدهنده به فیکسچر، توالی فیلم، مرحله تمیزکار日晚间، مالکیت فرآیند و برنامه جایگزینی کنید. یک دستگاه پولیش بدون نگهدارنده مناسب و مصرفیهای لازم، یک ایستگاه عملیاتی LC/SC محسوب نمیشود.
11. سطح انتهایی را تمیز و بازرسی کنید
پس از پولیش، کانکتور را با مواد تأییدشده تمیز کنید و آن را با استفاده از میکروسکوپ بازرسی کانکتور فیبر نوری همراه با آداپتور مناسب بررسی نمایید. سوابق پذیرش باید آلودگیهایی را که قابل تمیزکاری هستند از خطوط خراش، شکستگیها یا سایر عیوبی که نیاز به بازکاری یا رد شدن دارند، متمایز سازد.
مدل فنی 3D بر اساس میکروسکوپ بازرسی فِرول تأییدشده در سلول کاری LC/SC تأمینشده است. برند تأمینکننده حذف شده است.
IEC 61300-3-35:2022 covers visual inspection and classification of contamination, scratches and defects on fibre-optic connector interfaces. The product specification still needs to identify the applicable connector interface, inspection method and acceptance criteria. Visual inspection does not replace finished-product optical testing.
12. میزان تلفات درج و تلفات بازگشت را با 7420B اندازهگیری کنید.
The 7420B insertion-loss and return-loss tester is the final powered test station in the supplied package. Before FAT, define fiber type, wavelength, reference method, connector adapters, reference cords, test direction, acceptance limits, calibration responsibility and how each result is tied to the finished patch cord.
3D technical model based on the verified optical tester in the supplied package. Supplier branding has been removed; the station supports traceable insertion-loss and return-loss testing of the finished conventional patch cord.
IEC 61300-3-4:2023 روشهای اندازهگیری تضعیف را بررسی میکند، در حالی که IEC 61300-3-6:2008 addresses return-loss measurement procedures. These references do not supply the product’s pass/fail values; those values must come from the approved product specification and customer agreement.
13. بررسیهای نهایی چشمی را انجام دهید، برچسبگذاری و بستهبندی کنید
Use the visual fault locator when it belongs to the agreed work instruction, complete the final visual and dimensional checks, fit clean dust caps, apply the traceable label and pack the patch cord so the connector end faces and cable bend condition are protected. The released sample should carry the product code, length, connector configuration, fiber or cable identity, batch or serial reference and test status required by the buyer’s system.
The connector-processing area should be clean and have little airborne dust; a cleanroom is preferable when the product and quality requirements justify it. The layout must separate dirty preparation work from cleaned ferrules and finished connectors. The RFQ should assign compressed air, benches, lighting, cleaning materials, waste handling, labels and packaging instead of assuming they are included with the machines.
Pitfalls: The workcell depends on operator memory for strip length or polishing steps, end-face images are not tied to product identity, optical results have no documented reference method, or tested connectors are exposed to dust again before capping and packing.
خلاصه تجهیزات پشتیبان
| Process stage | Reference equipment | کنترل مجاور مورد نیاز |
|---|---|---|
| Length cutting | دستگاه برش خودکار کابل | سهم طول، تحمل و اندازهگیری نمونه |
| Jacket stripping | دستگاه ریسک کابل نوری | ابزارآلات و معیارهای آسیبدیدگی مخصوص کابل |
| Buffer stripping | دستگاه کندهکن روکش فشرده | بازرسی و تمیزکاری وضعیت فیبر |
| Adhesive preparation | Model 800 | ثبت هویت چسب، ترکیب و عمر قابل استفاده |
| Adhesive dispensing | Epoxy dispenser | دوز، آداپتور و کنترل تمیزکاری |
| Connector crimping | دستگاه کریمپ پنوماتیک | قالب اختصاصی کانکتور و هوای فشرده |
| Curing | کوره عملآوری کانکتور | قابلیت ردیابی چرخه و دستهای تأییدشده |
| Ferrule polishing | دستگاه صیقلدهی سوکت فیبر | فیکسچر LC/SC، فیلمها و توالی تمیزکاری |
| بازرسی سطح انتهایی | میکروسکوپ بازرسی کانکتور فیبر | آداپتور، معیارها و نتیجهی قابل ردیابی |
| Optical testing | 7420B | طول موج، تنظیمات مرجع، حدود و کالیبراسیون |
کدام وسایل، ابزارها و مصرفیها در RFQ گنجانده شوند؟
Fixtures and consumables are part of the manufacturing system because they determine which connectors can be processed and whether the result is repeatable. A machine without the correct holder, film, adapter or cleaning control is not a complete station.
Peter’s supplied package names LC and SC polishing fixtures, including UPC and APC variants where applicable. FC and ST fixtures are also available in the reference package, but they should be added only when those connector families belong to the approved product list. The package also includes fiber and cable strippers, crimping pliers, aramid scissors, a fiber cutting pen, an electronic balance, adhesive, polishing pads and films, a visual fault locator and cleaning paper.
| Scope group | موارد برای زمانبندی | تصمیم خریدار |
|---|---|---|
| Connector fixtures | نگهدارندههای پولیش، آداپتورهای بازرسی، آداپتورهای تست و هرگونه فیکسچر کریمپ یا مونتاژ | هر خانواده کانکتور، نوع انتهای فِرول و تأمینکننده قطعه را فهرست کنید |
| ابزارهای دستی آمادهسازی | دستگاه کندهکن فیبر، دستگاه کندهکن روکش، قیچی آرامید، ابزار برش و انبردست خمکننده | تعیین مقدار جایگزینی، تخصیص اپراتور و روش بازرسی |
| Adhesive controls | چسب، ابزارهای وزنکردن یا مخلوطکردن، سانتریفیوژ، دستگاه توزیعکننده و لوازم نظافتی | سیستم چسب سازگار و کنترلهای ذخیرهسازی، آمادهسازی و عمر قابل استفاده را منجمد کنید |
| Polishing consumables | پدها، فیلمها و مواد تمیزکننده | تایید توالی، گرید، تأمینکننده، قاعده تغییر و کنترل لات |
| Test accessories | کابلهای مرجع، آداپتورها، ماندرلها یا قطعات شرطسازی مد در صورت نیاز و محلیاب خطای بصری | روش آزمون، رابطهای کانکتور و مالکیت کالیبراسیون را تعریف کنید |
| Finishing materials | کلاهکهای گرد و غبار، برچسبها و مواد بستهبندی | تعیین تمیزی، هویت، ارائه و محافظت در حمل و نقل |
What to ask: Require a connector-to-fixture matrix and a consumable list for the launch products. The supplier should state which items are included, which wear out, which require regular replacement and which must be sourced from the connector or consumable manufacturer.
آیا یک کارخانه جدید باید کابل پایه را خریداری کند یا در داخل تولید کند؟
Start with the narrowest complete route that can release the intended saleable patch cord. Buying qualified cable concentrates investment and training on connector assembly; adding HK-30 and HK-50 brings cable construction and supply control in house but also adds extrusion, material, reel and intermediate-quality responsibilities. گستردهتر نقشه مسیر تولید کابل فیبر نوری به خریداران کمک میکند تا این مسیر کابل داخلی باریک را در کنار سایر خانوادههای خط کابل نوری قرار دهند بدون اینکه یک فهرست ماشین را بهعنوان جهانی در نظر بگیرند.
| Decision factor | کابل پایهی واجد شرایط را خریداری کنید | افزودن تولید کابل پایه درونسازمانی |
|---|---|---|
| محدوده فرآیند اولیه | تأیید کابل ورودی به همراه مونتاژ کانکتور | پردازش بافر فشرده، آرامید و روکش بهعلاوه مونتاژ کانکتور |
| کنترل تأمینکننده اصلی | کشش کابل، سوابق قرقره و اطلاعیه تغییر | الیاف، ترکیبات، ابزارها، دستورالعملها، ردیابی کابل در حال تولید و قرقره |
| مهارتهایی برای توسعه | آمادهسازی، اتصال، پولیش، بازرسی و آزمون نوری | تمامی مهارتهای مونتاژ به علاوه اکستروژن، خنککاری، کنترل کشش و کنترل پیچش |
| Expansion constraint | پرتفوی تأمینکنندگان تأییدشده و شرایط زمان انتظار | پنجره تجهیزات، ابزارآلات، مواد و برنامه تعویض تأیید شده |
| Handoff risk | تأیید ردیف ورودی به کارنامه مونتاژ | خروجی HK-30 به HK-50، سپس قرقره نهایی به مونتاژ کانکتور |
Decision criterion: Compare the approved product mix, cable-source reliability, process knowledge, staffing, quality system and traceability burden. Do not justify the integrated route only with an unsupported production-volume or payback threshold.
Red flags: A proposal adds cable extrusion without an intermediate-reel release plan, or assumes that owning the cable line automatically reduces finished-patch-cord defects. Control improves only when materials, work instructions, operators and evidence are qualified together.
چرا MPO از این مسیر تجهیزات حذف شده است؟
MPO is excluded because both its incoming multi-fiber cable and its connector-assembly workcell can differ from conventional single-fiber patch cords. A polishing fixture alone does not convert the ordinary patch-cord route into an MPO route.
The supplied specialist catalog separates the ordinary patch-cord machines from a dedicated MPO/MTP group. That group includes multi-fiber-specific preparation, polishing fixtures, curing, end-face or geometry inspection, polarity or channel control and multi-channel optical testing. Peter’s supplied experience also identifies more stable automatic polishing pressure as an important MPO consideration because one connector presents multiple fibers to the polishing process.
This article therefore stops at conventional single-fiber connector families. A separate MPO article must begin with the exact cable construction, fiber count, ferrule and connector system, polarity, end-face geometry requirement and channel-test method before selecting equipment.
Note: The supplied conversation mentions a project range of multiple fibers per MPO connector. That range remains a bounded project observation and will not be published as a universal MPO specification without Peter’s confirmation.
RFQ و FAT باید چه چیزی را اثبات کنند؟
The RFQ must describe the complete route and responsibility boundary. FAT should use representative finished LC and SC patch cords from the approved launch range and prove them through the selected cable, connector, fixture, consumable, inspection and optical-test system.
| Acceptance layer | RFQ document | FAT evidence |
|---|---|---|
| Finished product | کشش کابل، اجزای کانکتور، نوع فیبر، طول، پرداخت نهایی و برچسب | نمونه شناساییشده با پیکربندی تأییدشده مطابقت دارد |
| مرز مسئولیت | ماتریس HONGKAI-ساختهشده، تخصصی-ادغامشده، تأمینشده توسط خریدار و مورد مستثنی | هر ایستگاه، تأسیسات و آزمون دارای یک مالک و وضعیت مورد باز است |
| کابل پایه در صورت ارائه | مصالح، ابزارها، دستورالعملها، بستهبندی و برنامه انتشار | کلافهای بافر فشرده و کابل نهایی قابل ردیابی همراه با سوابق ابعادی و نوری توافقشده |
| Cable preparation | دستورالعملهای کار برش و رشتهگیری | طول اندازهگیریشده، وضعیت انتهای آمادهشده و هویت مسافر |
| Connector assembly | دستورالعملهای قطعه، چسب، کریمپ و عملآوری | لотов کامپوننت و مصرفی، تنظیمات و سوابق چرخه |
| صیقل دادن و بازرسی | ماتریس اتصالدهنده به فیکسچر، توالی فیلم و معیارهای بازرسی | نتیجه قابل ردیابی انتهای سطح برای هر نمونه FAT |
| Optical test | طول موج، تنظیمات مرجع، حدود، جهت و نمونهبرداری | نتایج ثبتشده تلفات درج و تلفات بازگشت هنگام نیاز |
| Work environment | سطح نظافت، کنترل گردوغبار، هوای فشرده و شرایط میز کار | Back-end area is clean, low in airborne dust and suitable for the agreed connector process |
| بستهبندی و برچسبها | درپوشهای ضد گرد و غبار، فیلدهای برچسب، روش بستهبندی و تأمینکننده مسئول | Released sample has the agreed identity, protection and presentation |
| Handover and training | Layout, utilities, manuals, calibration, spares, consumables and training split | HONGKAI اپراتورها را بر روی تجهیزات HONGKAI آموزش میدهد؛ شریک ادغام، اپراتورها را بر روی تجهیزات شریک آموزش میدهد |
بررسینامه:
- ☐ Launch products and connector families are listed separately
- ☐ Cable-making and connector-assembly scopes are separated
- ☐ Every machine, fixture, adapter and consumable has a named product purpose
- ☐ HONGKAI-manufactured, specialist-integrated and buyer-supplied items are explicit
- ☐ مؤلفههای فیبر ورودی، کابل، کانکتور و مصرفیها دارای قوانین تأیید هستند
- ☐ End-face inspection and optical testing are both included where required
- ☐ FAT samples use the agreed cable, connectors, fixtures and work instructions
- ☐ ناحیه بکاند، هوای فشرده، بستهبندی و برچسبها دارای مالکان مشخص هستند
- ☐ Training, calibration, maintenance and traceability ownership are assigned
Evidence to request: Keep the approved drawings, equipment configuration, material and component lots, work instructions, operator identity, settings, cure and polish records, inspection images, optical-test setup, raw results, sample labels and a dated open-item list. The separate راهنمای نصب و راهاندازی خط فیبر نوری provides a broader acceptance framework for utilities, documentation, startup and handover.
Note: The complete patch-cord production route is the smallest connected system that can turn approved inputs into a repeatable, traceable finished product. Equipment count alone does not prove that the route is complete.
