Cable release
Manufacture and release the MPO base cable.
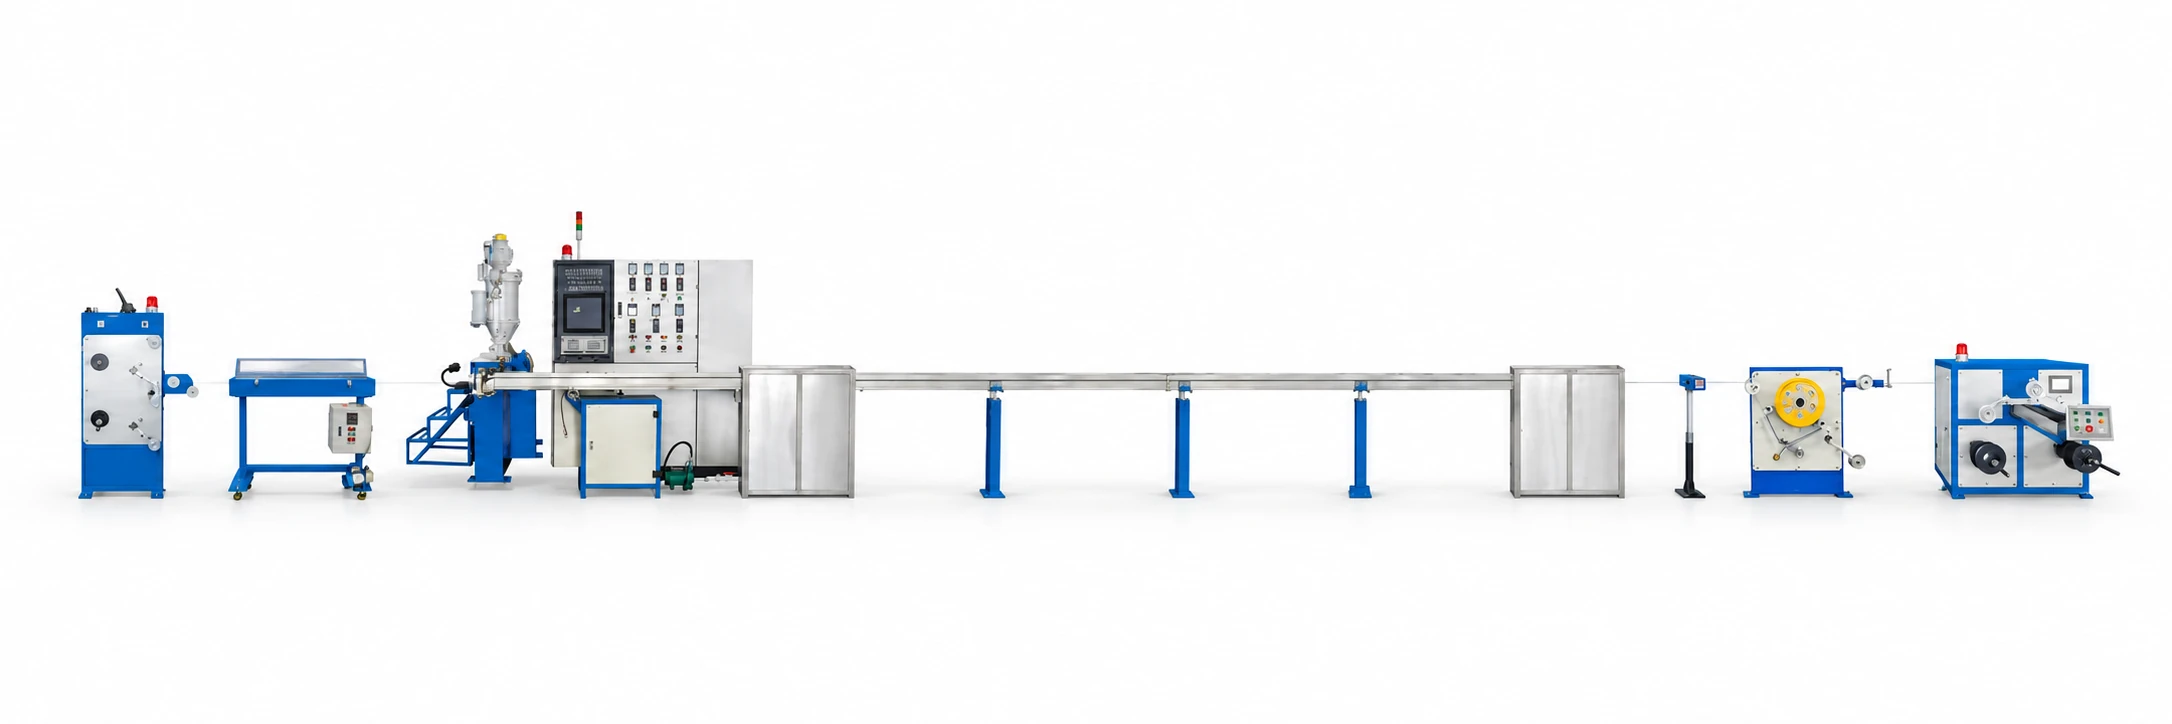
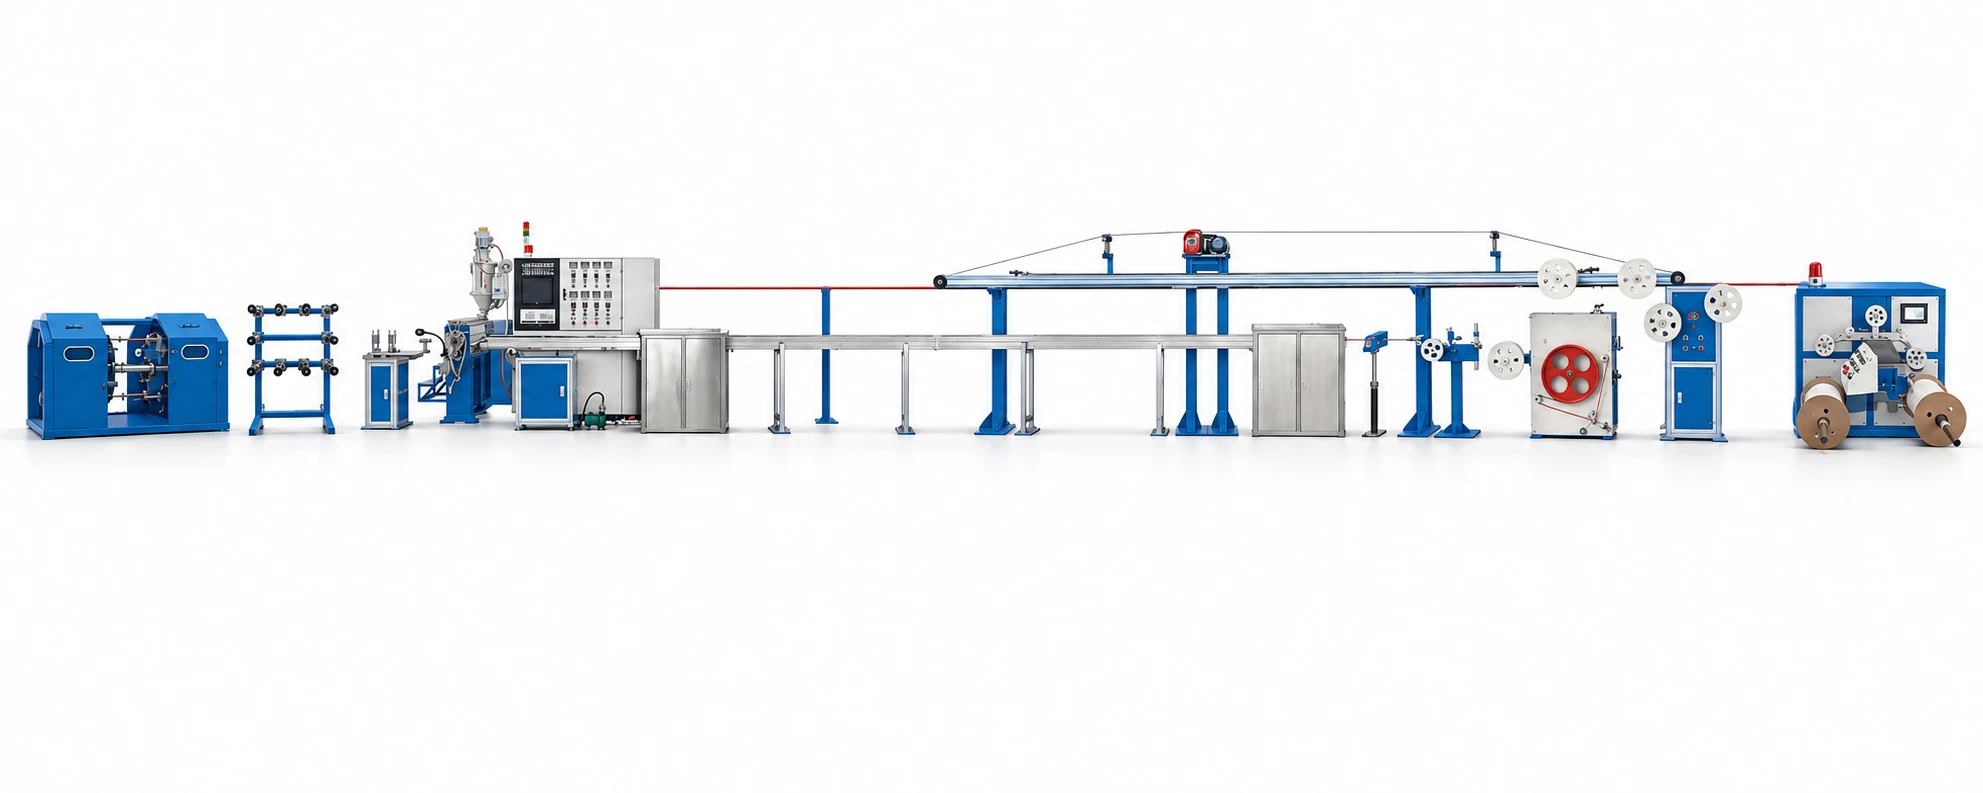
- HK-30 buffering and configured GJFJV jacketing
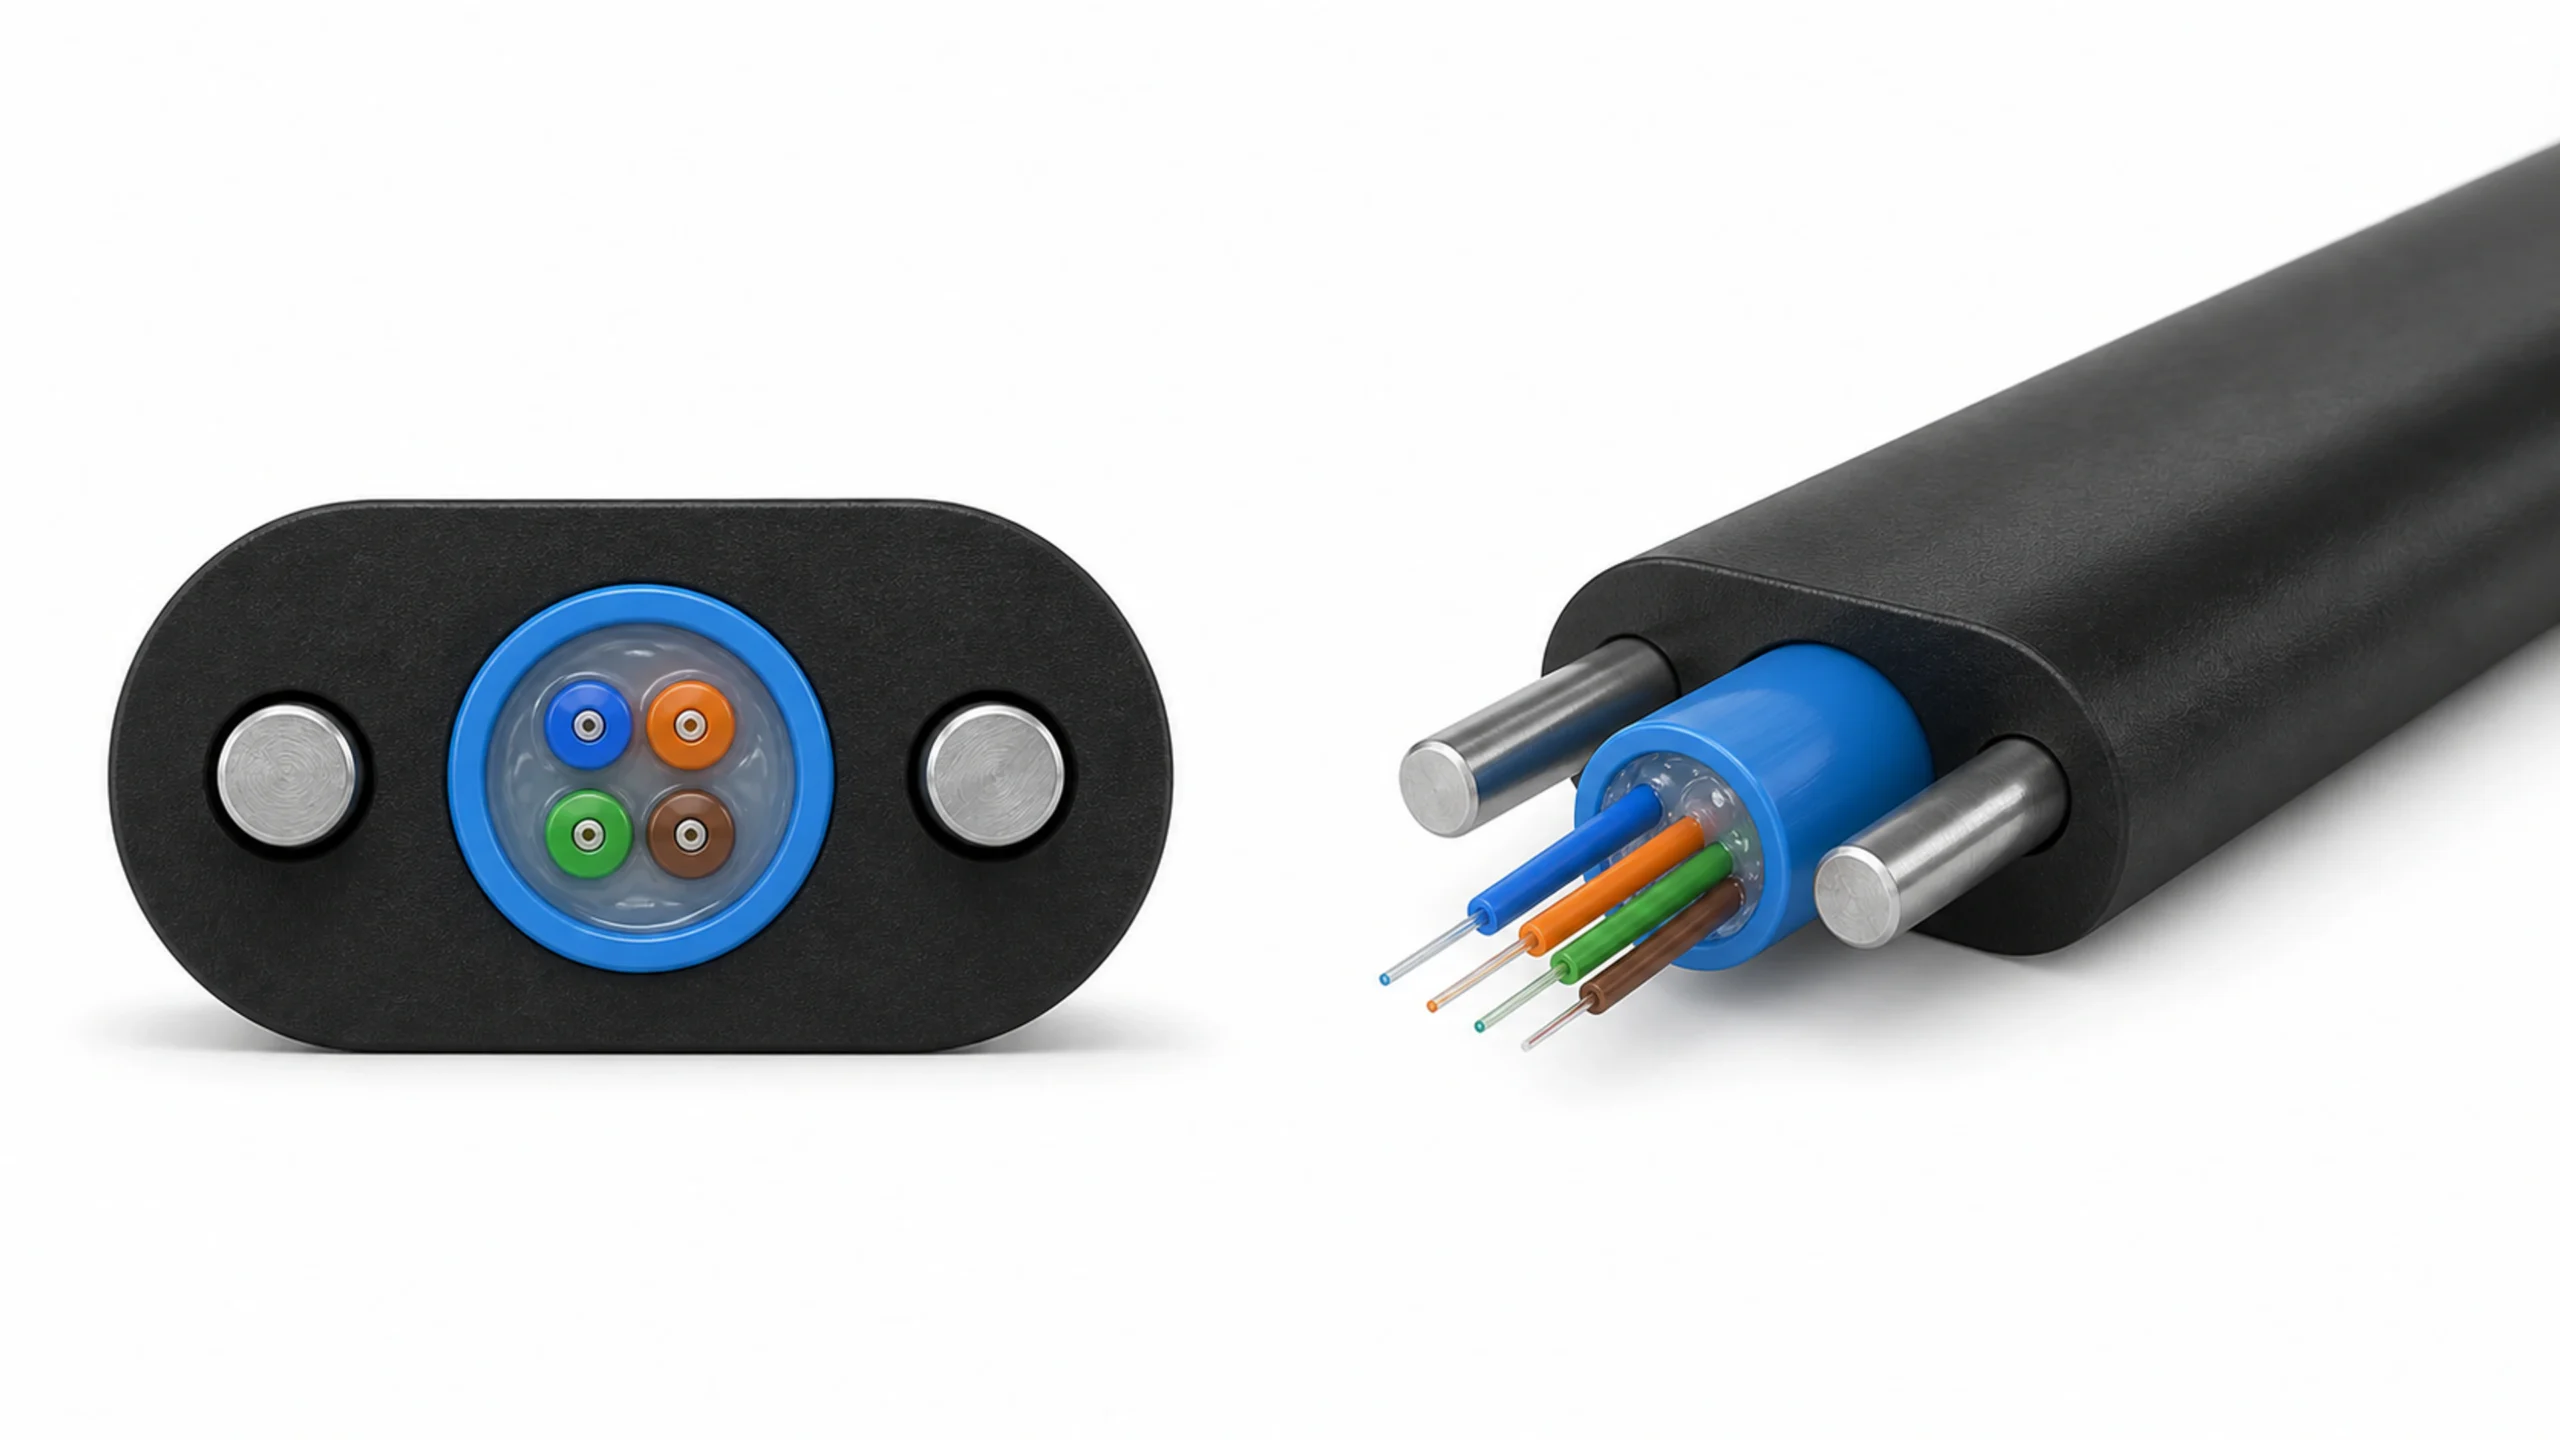
- Verified cable structure, dimensions and fiber identification
- Optical and agreed mechanical release records
ماشینآلات کابل
تجهیزات ساخت کابل نوری
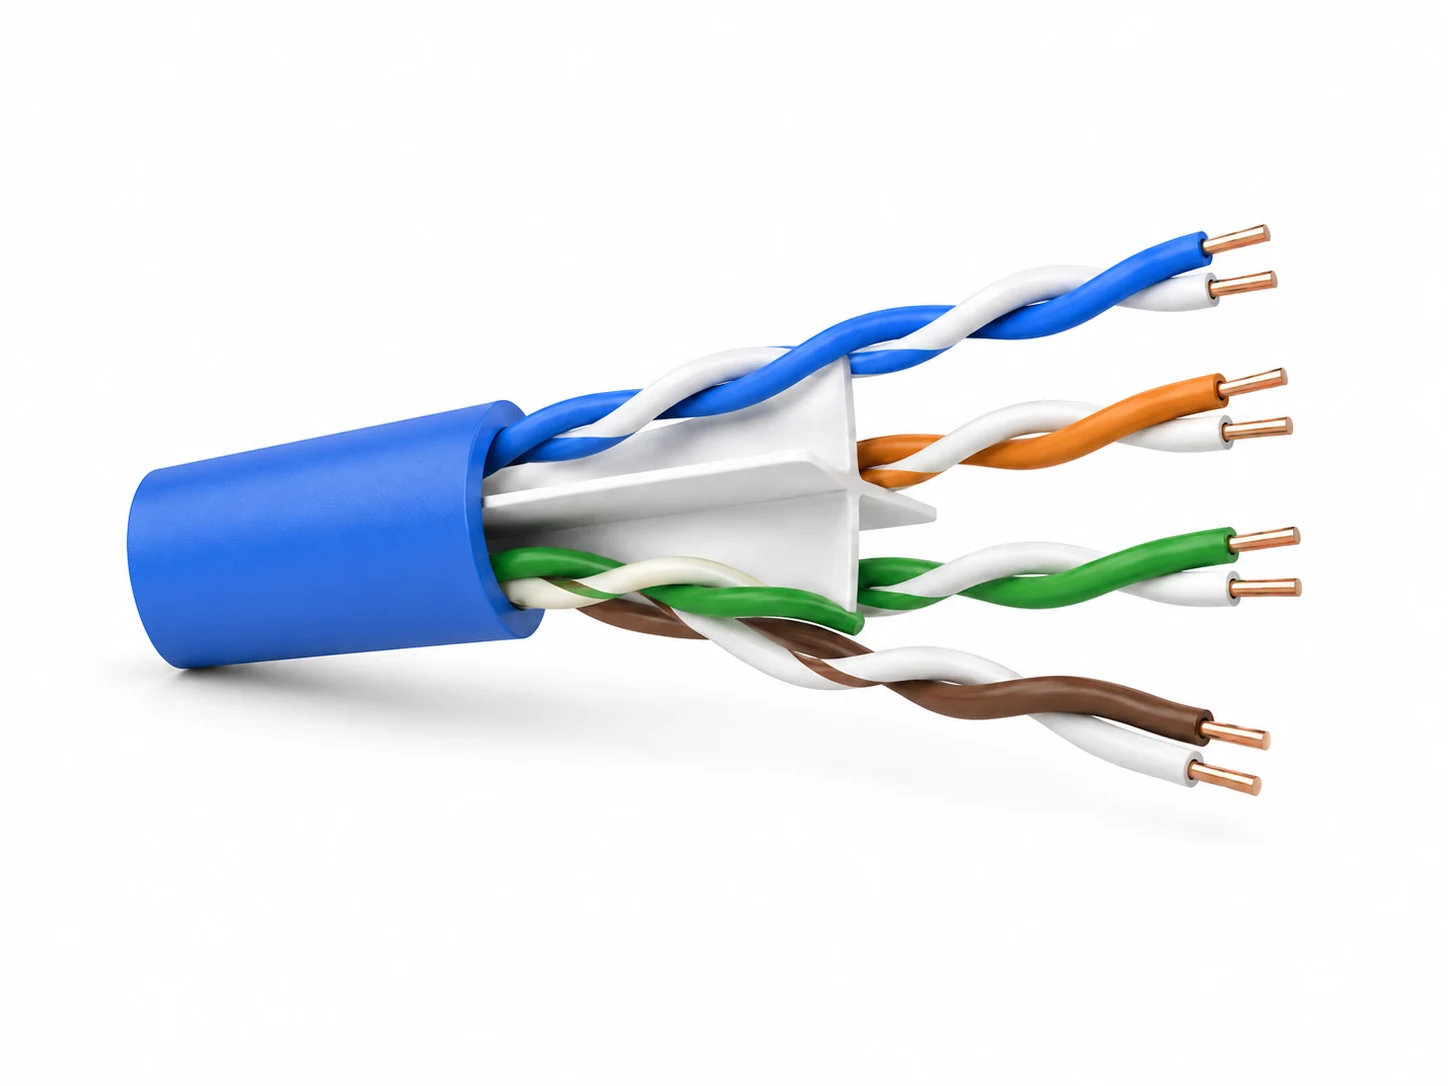
تجهیزات کابل زوج بههم تابیده
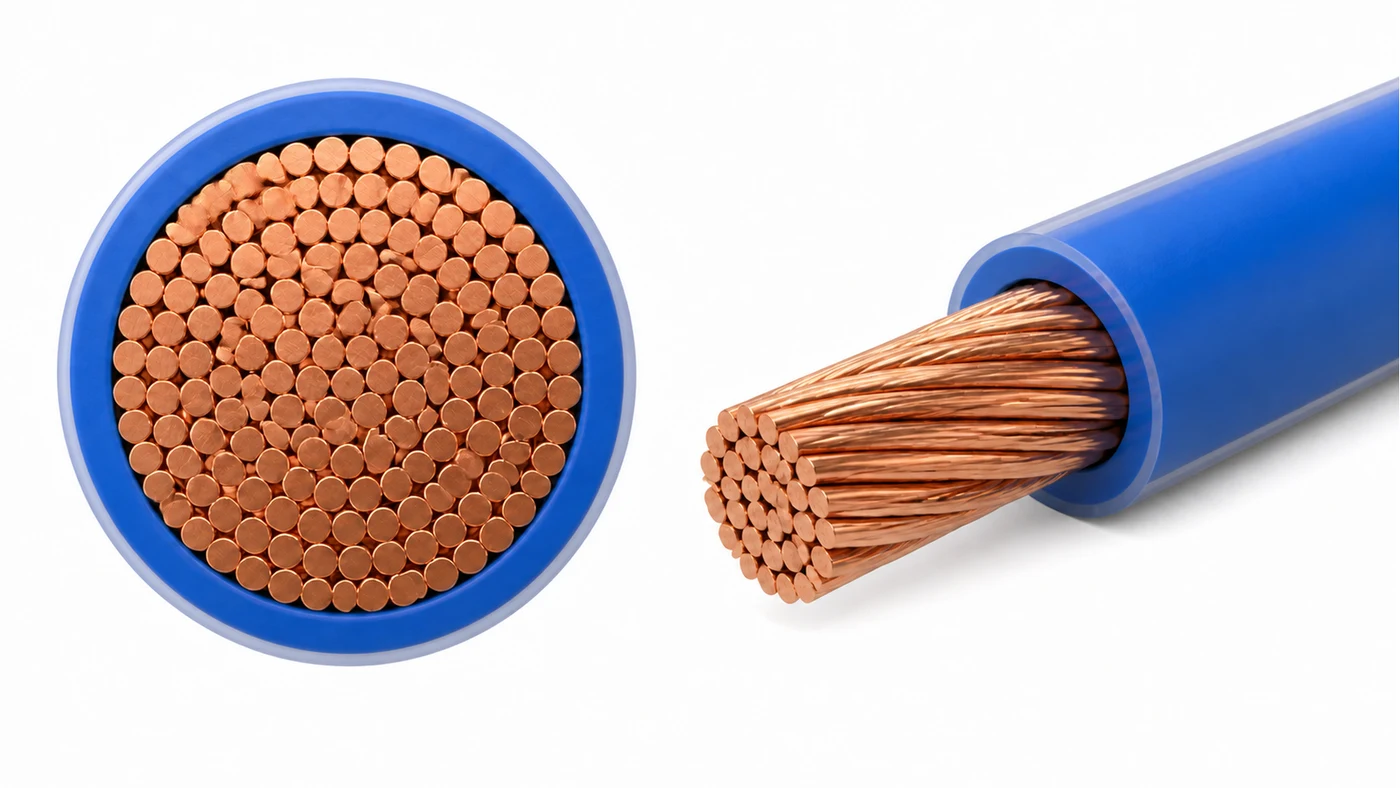
ماشینآلات سیم و کابل عایقدار
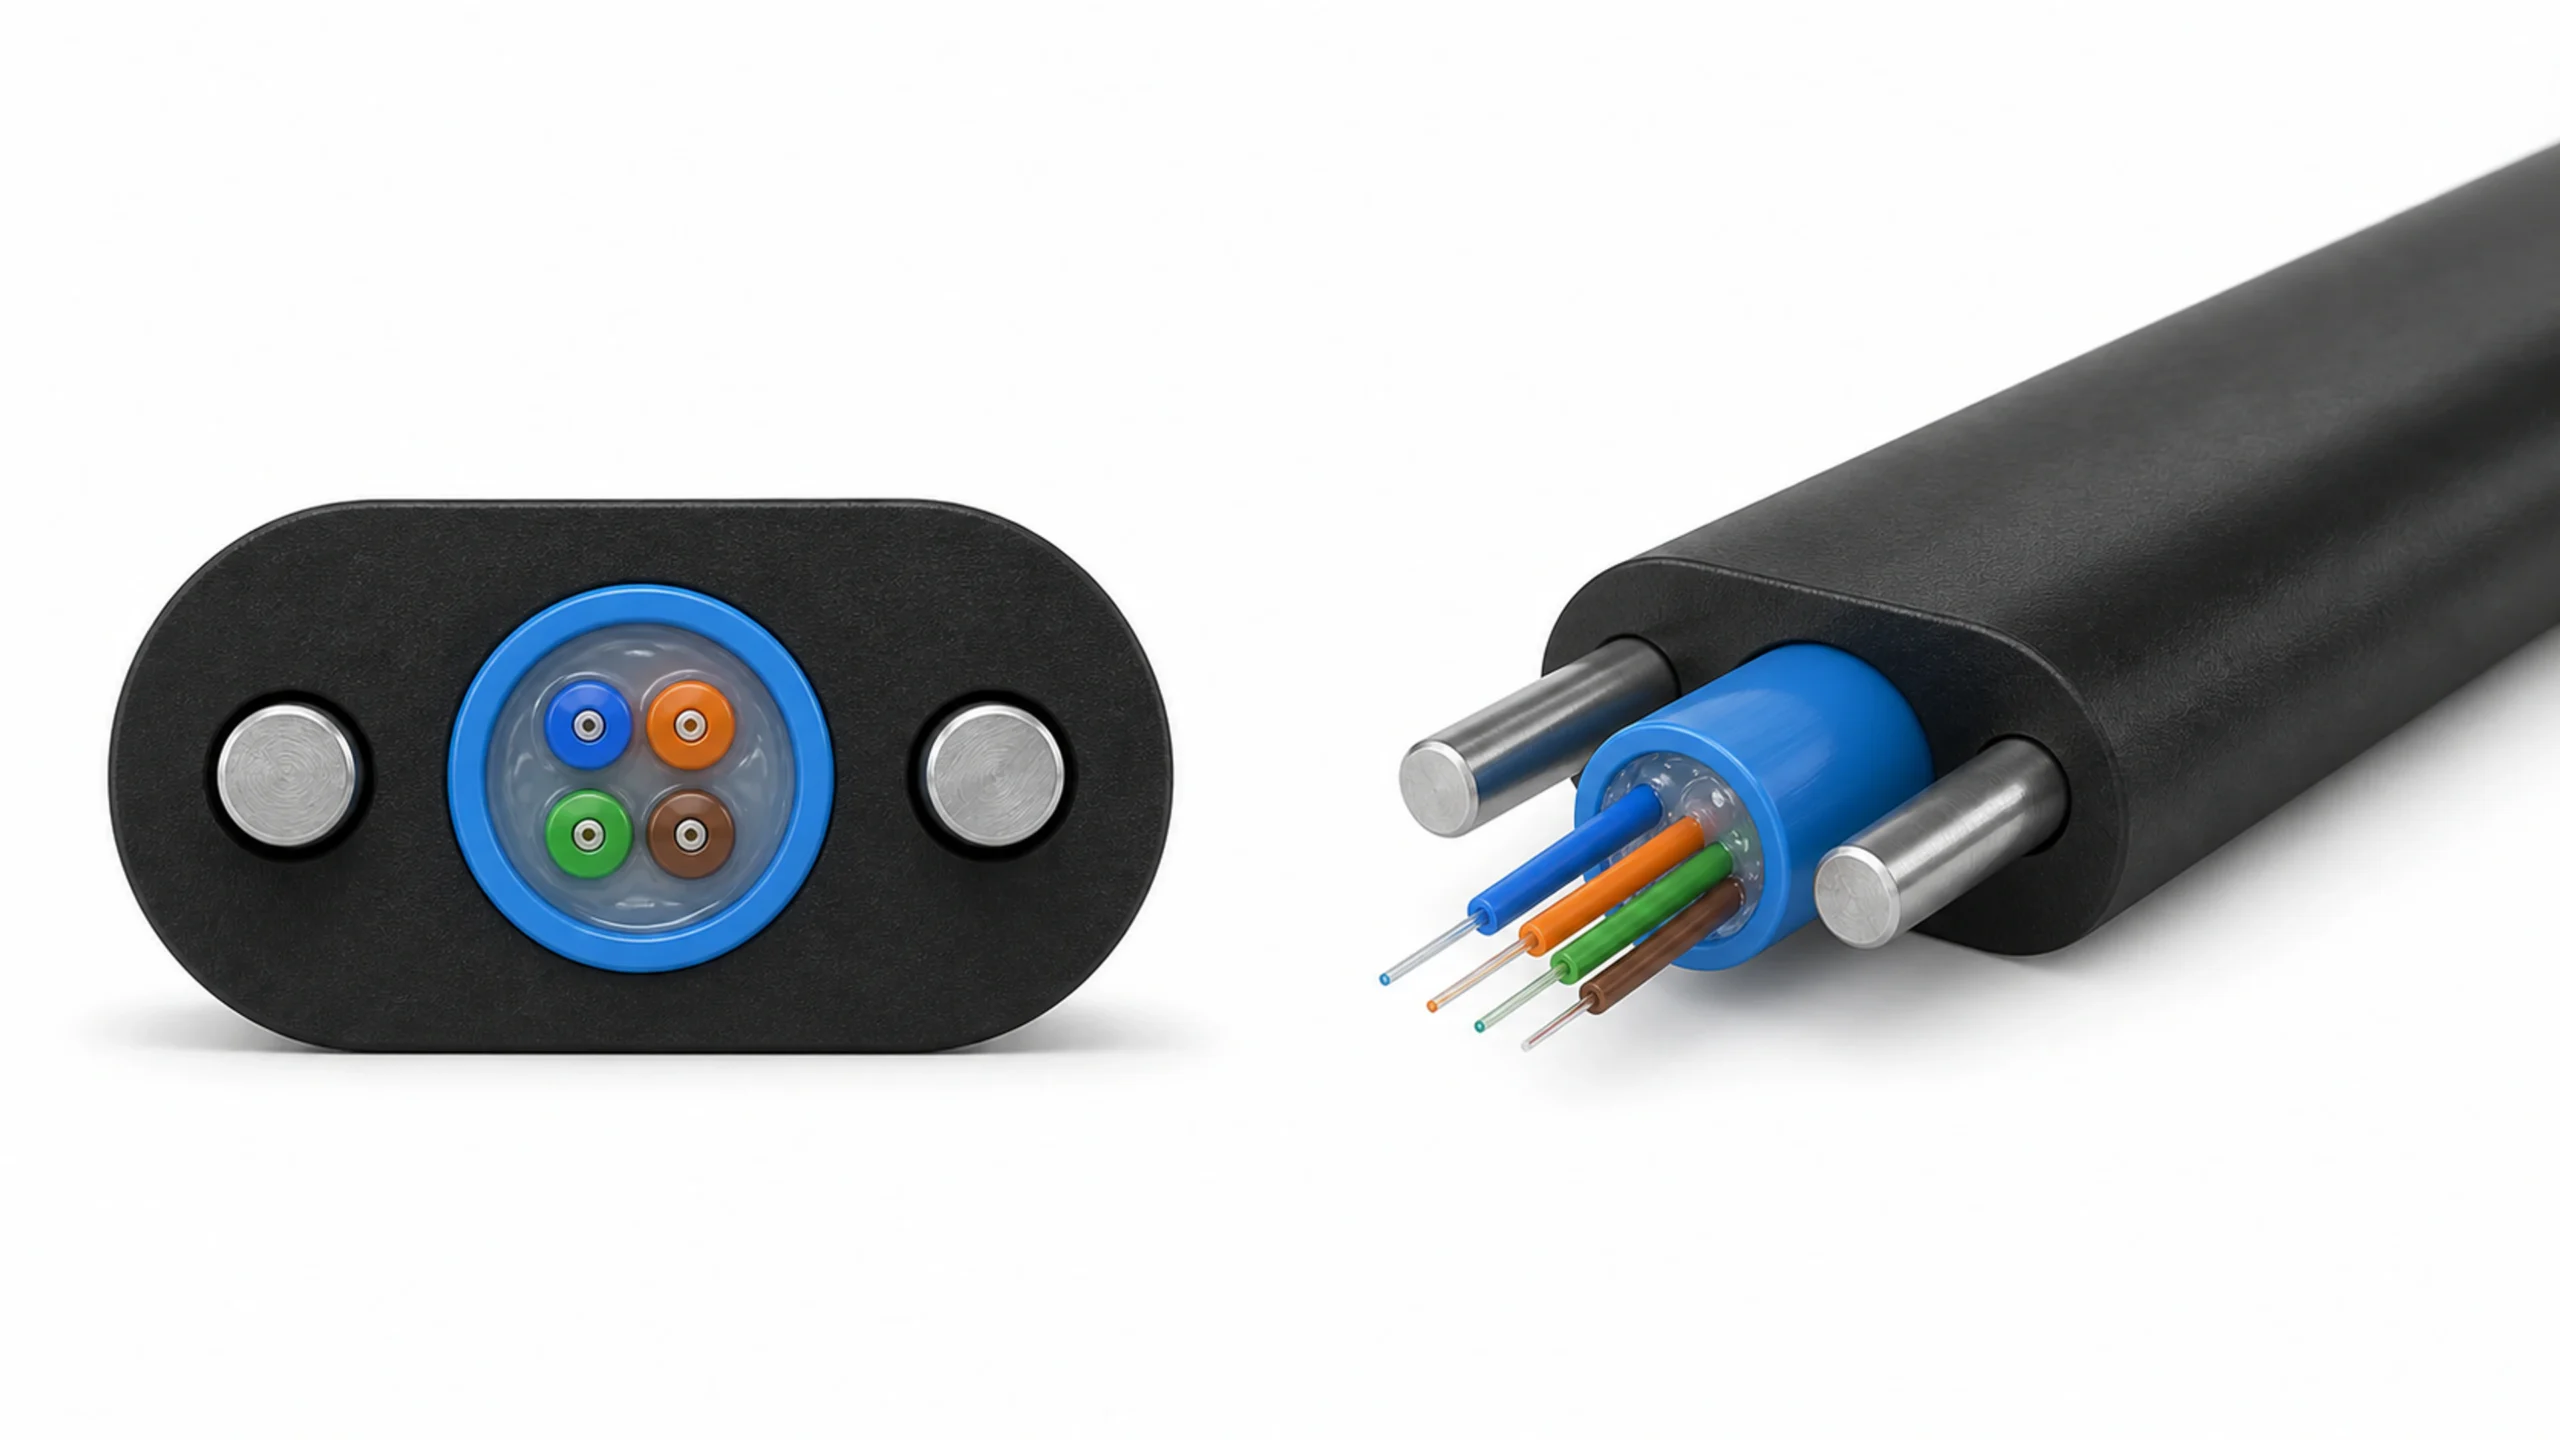
انواع کابل فیبر نوری را مرور کنید
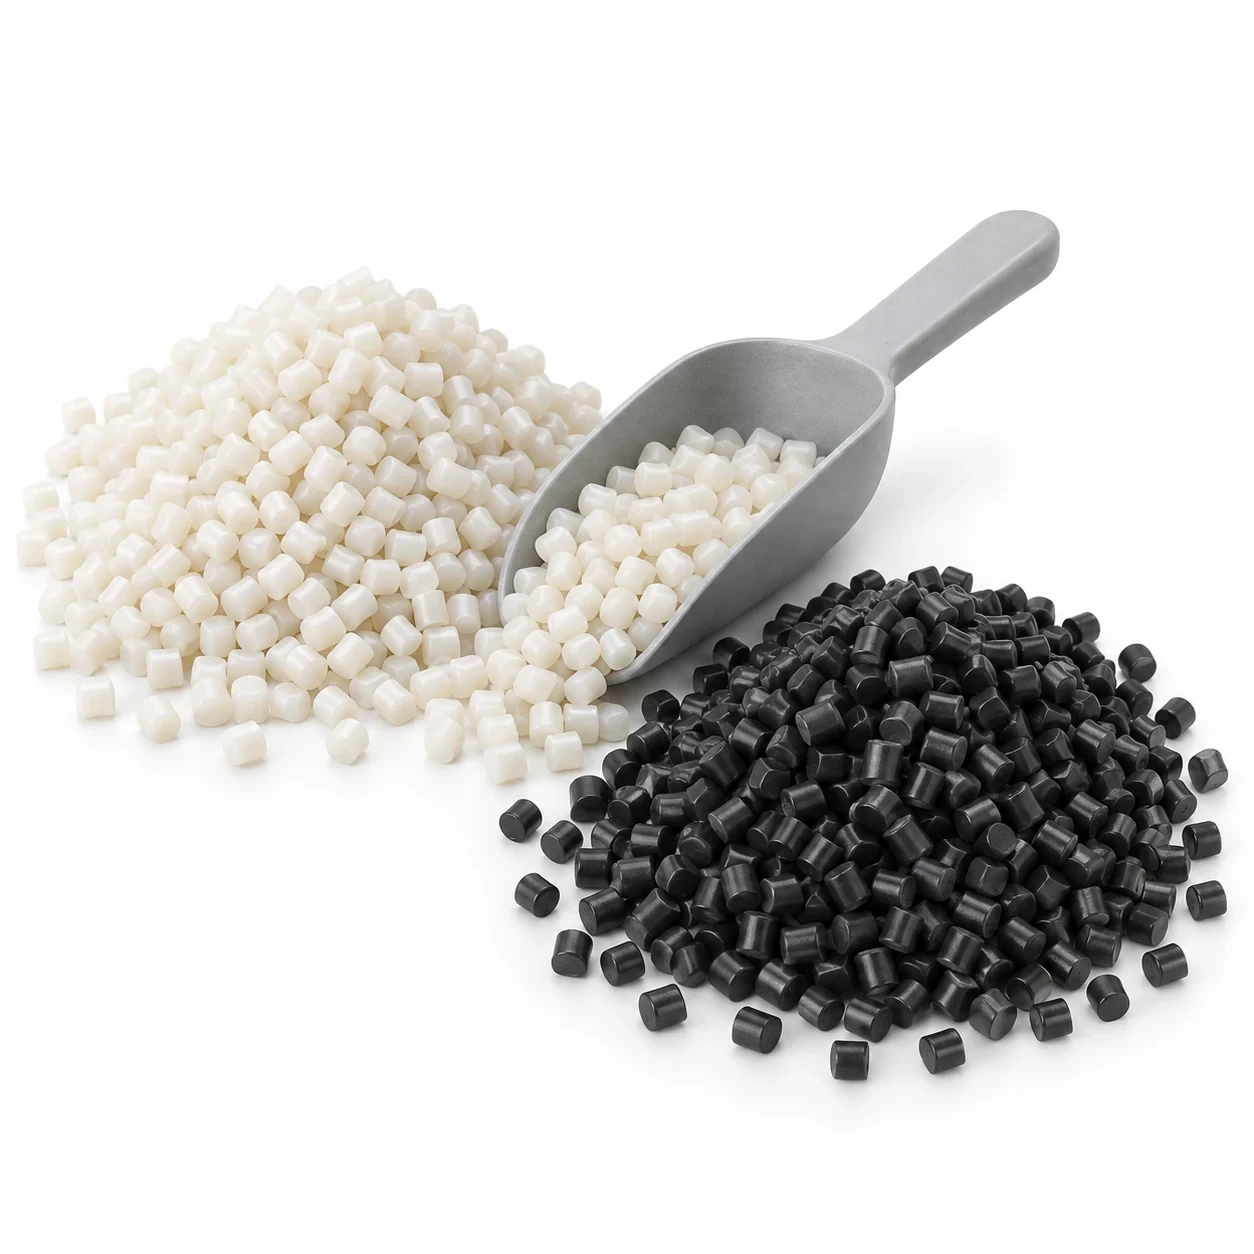
مواد مورد نیاز برای تولید کابل نوری
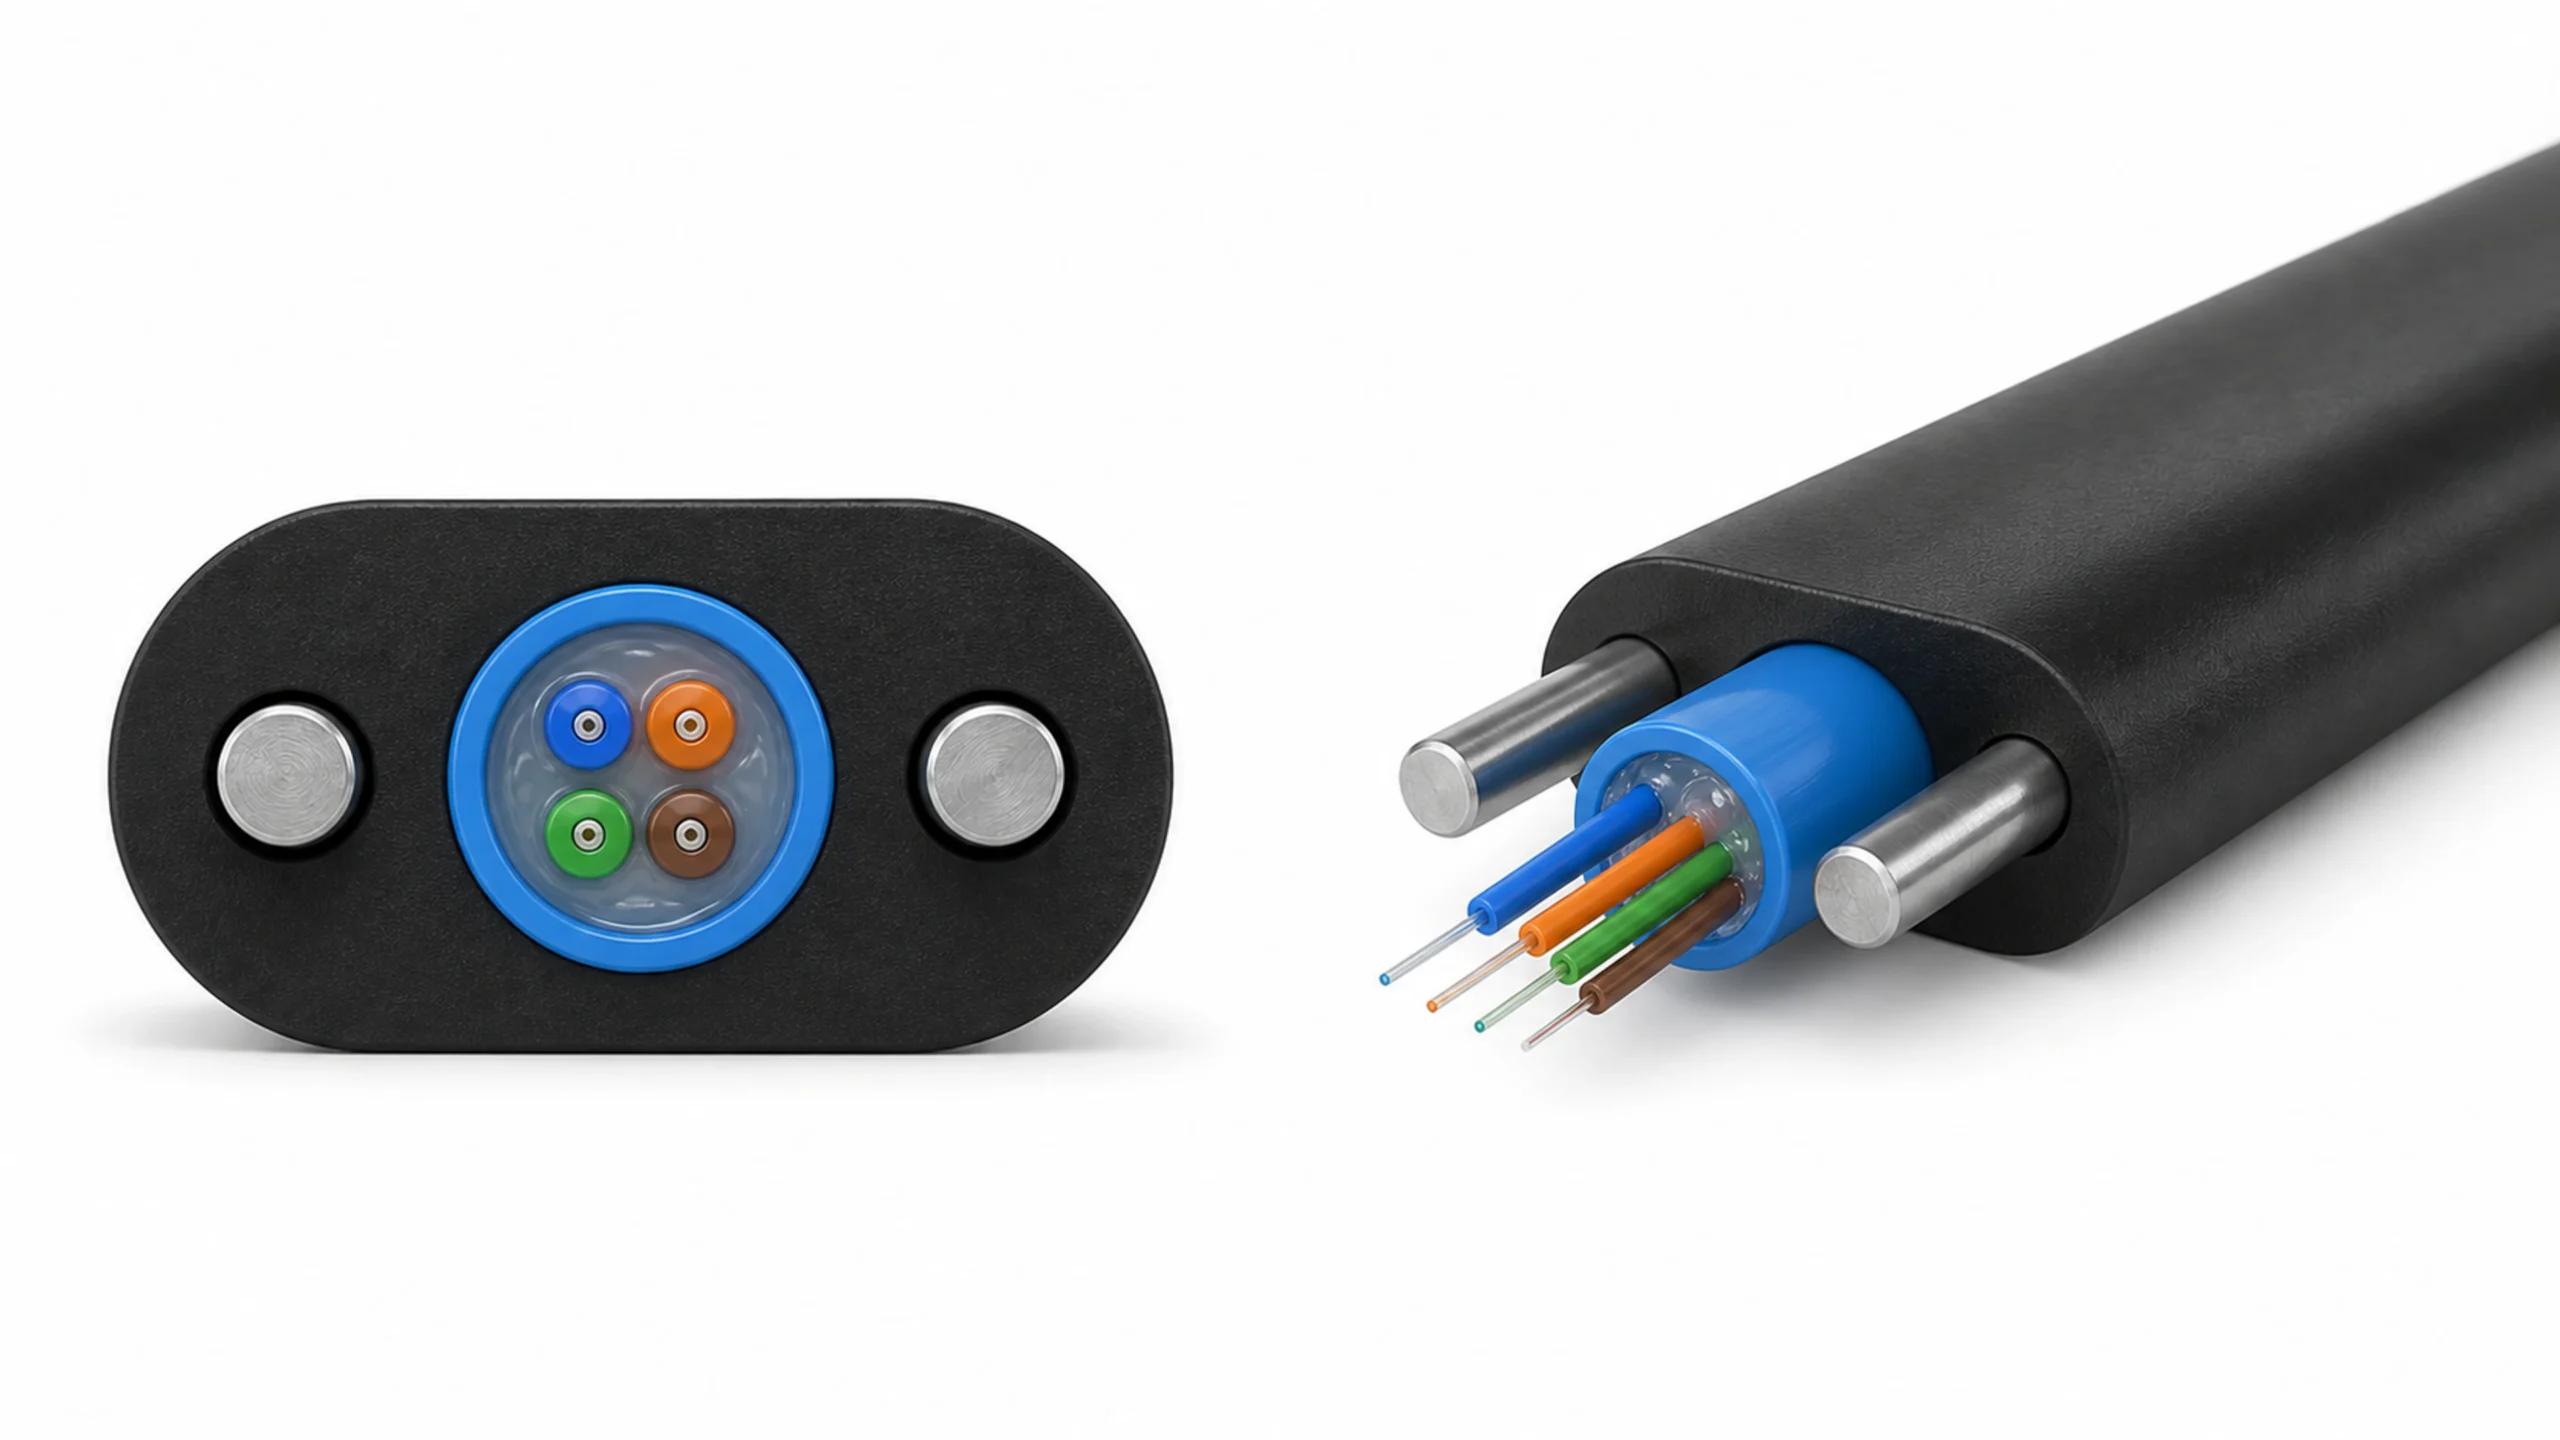
خطوط کامل کابل، مواد، چیدمان و پشتیبانی راهاندازی.

تولید کابل، مونتاژ MPO و آزمون نوری نهایی.
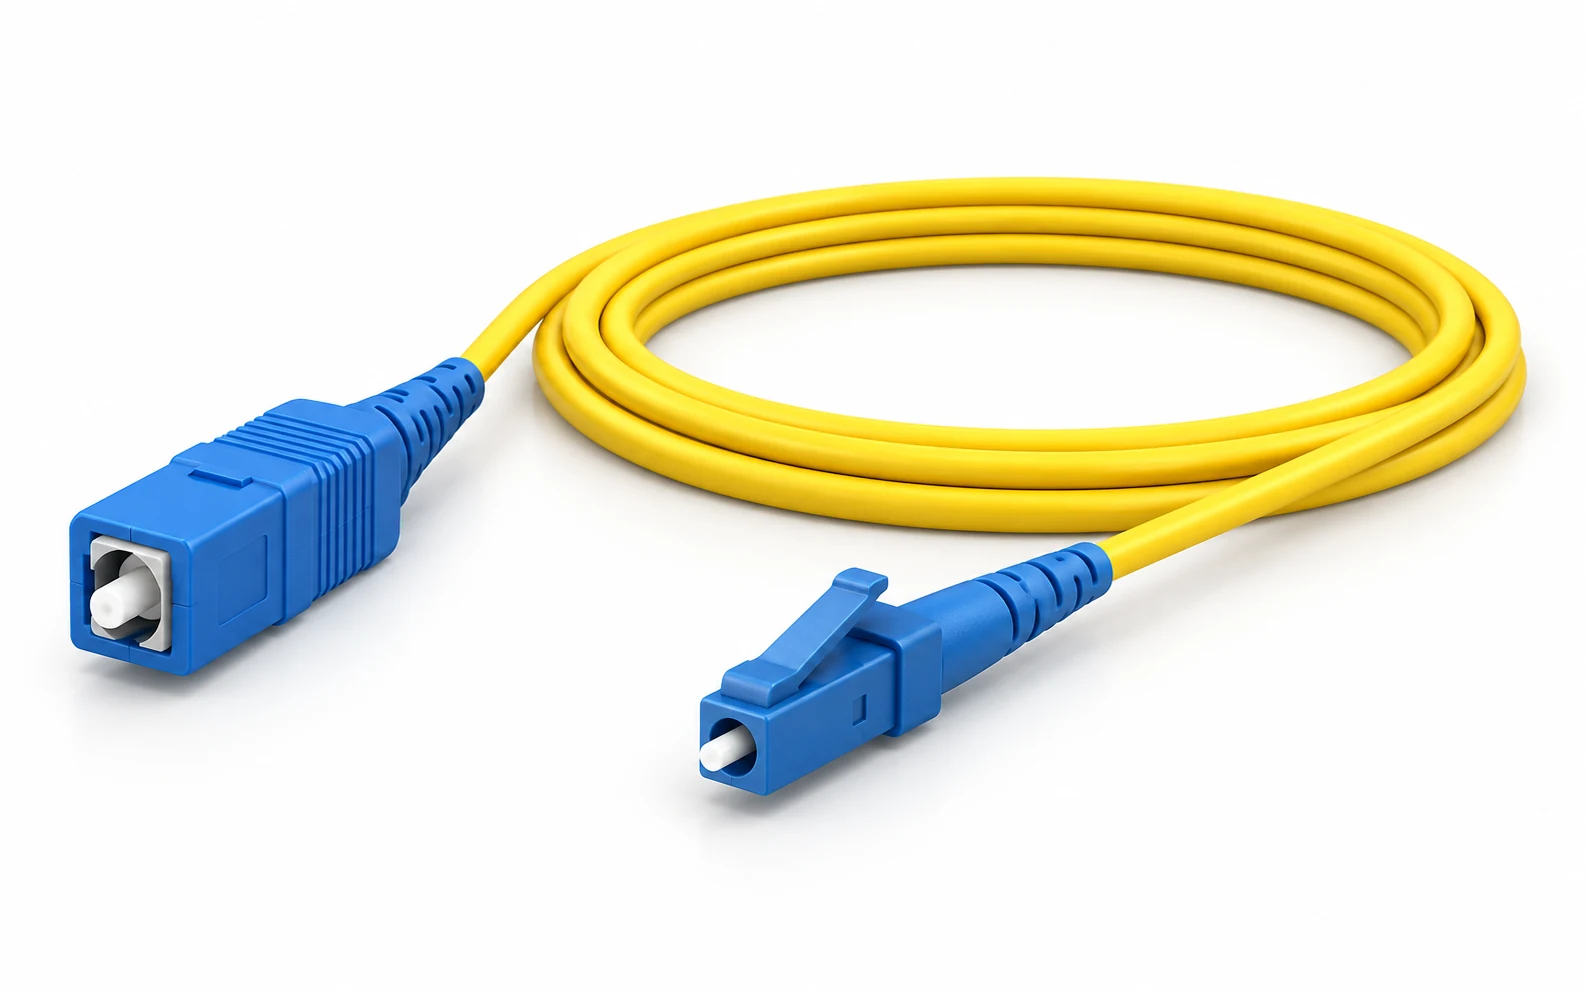
کابل پایه، مونتاژ کانکتور، پولیش و تحویل.
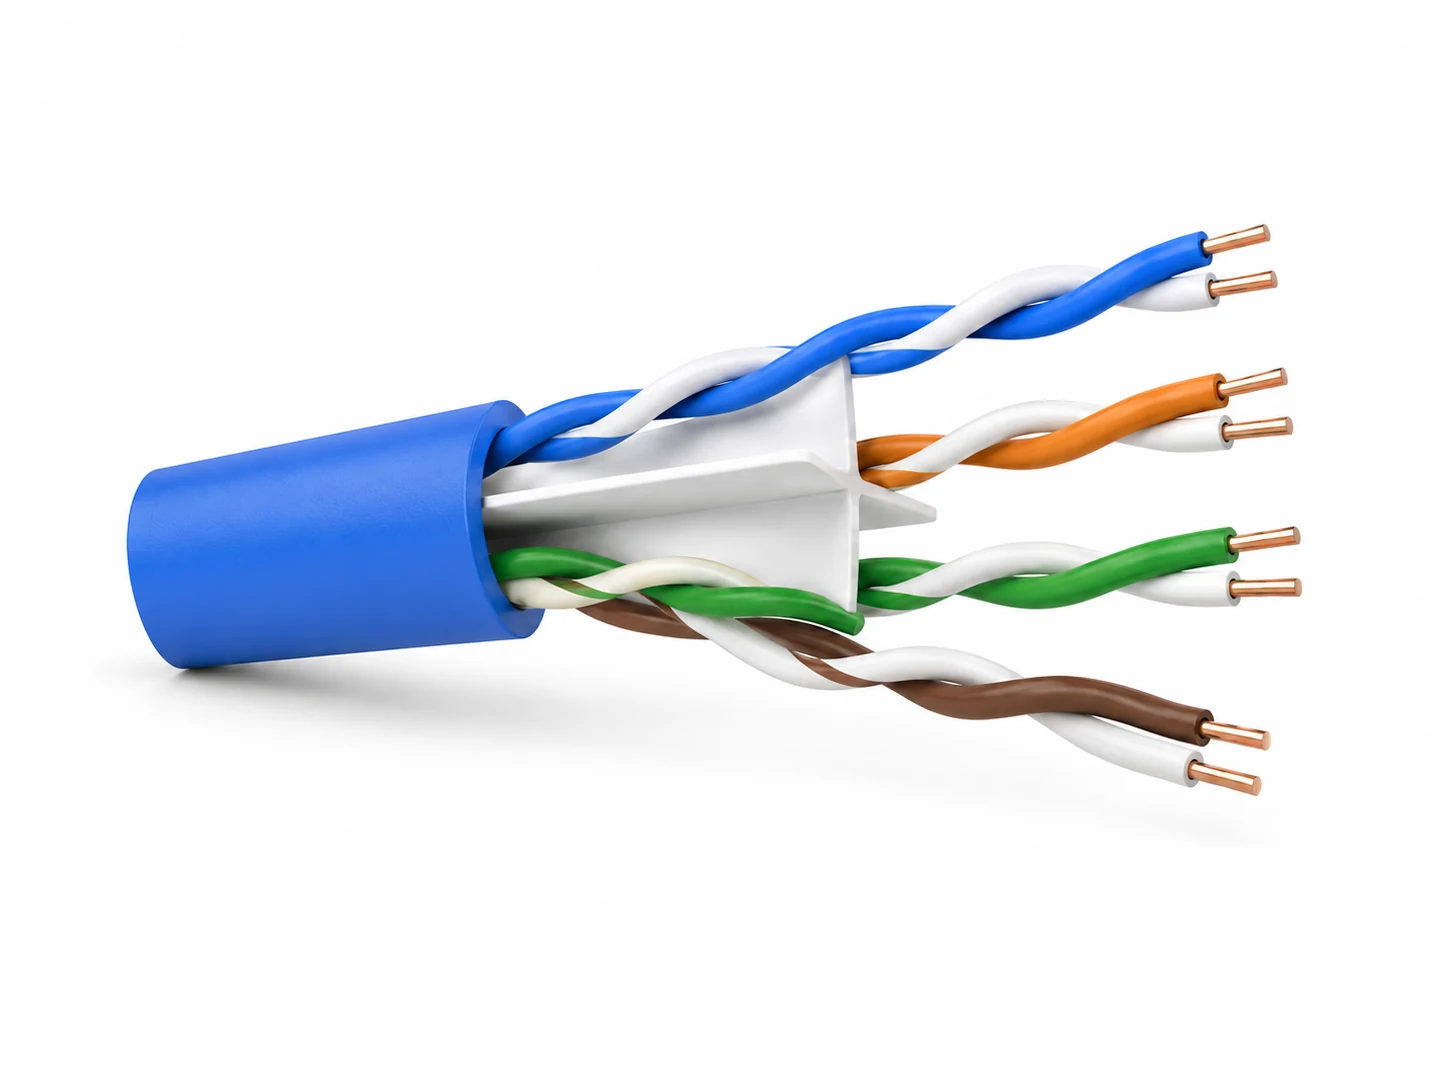
انتخاب تجهیزات و برنامهریزی فرآیند برای کابل شبکه.

01MPO CABLE & ASSEMBLY FACTORY SOLUTION
از فیبر نوری تا یک مجموعه MPO آزمایششده.
یک راهحل کامل کارخانه شامل تجهیزات، مواد، چیدمان و دانش فنی برای تولید کابل و مونتاژ دقیق MPO.
For new factories, existing cable manufacturers and assembly businesses ready to expand.
Plan My MPO FactoryExplore the full process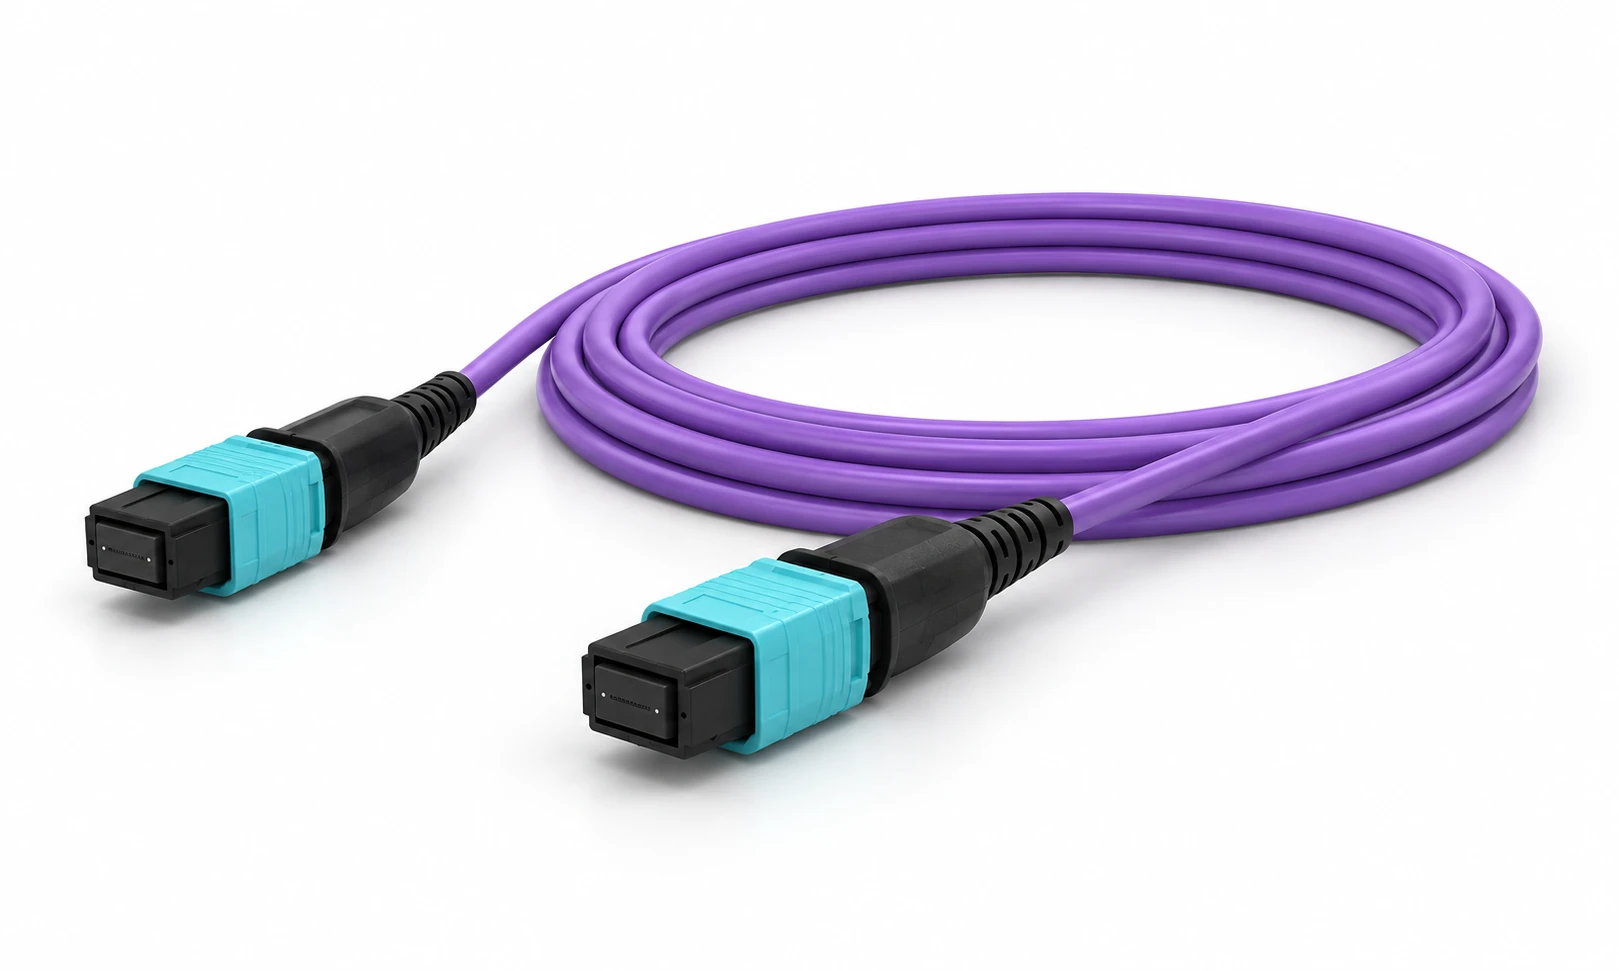
Illustrative reference.
Final scope follows the
approved product.
02INTERACTIVE PROCESS EXPLORER
See what to make, which areas are required, and how each step fits into a complete MPO factory.
STAGE 04 / 07
Individual fibers are separated, identified and arranged into a linear array for MPO termination.
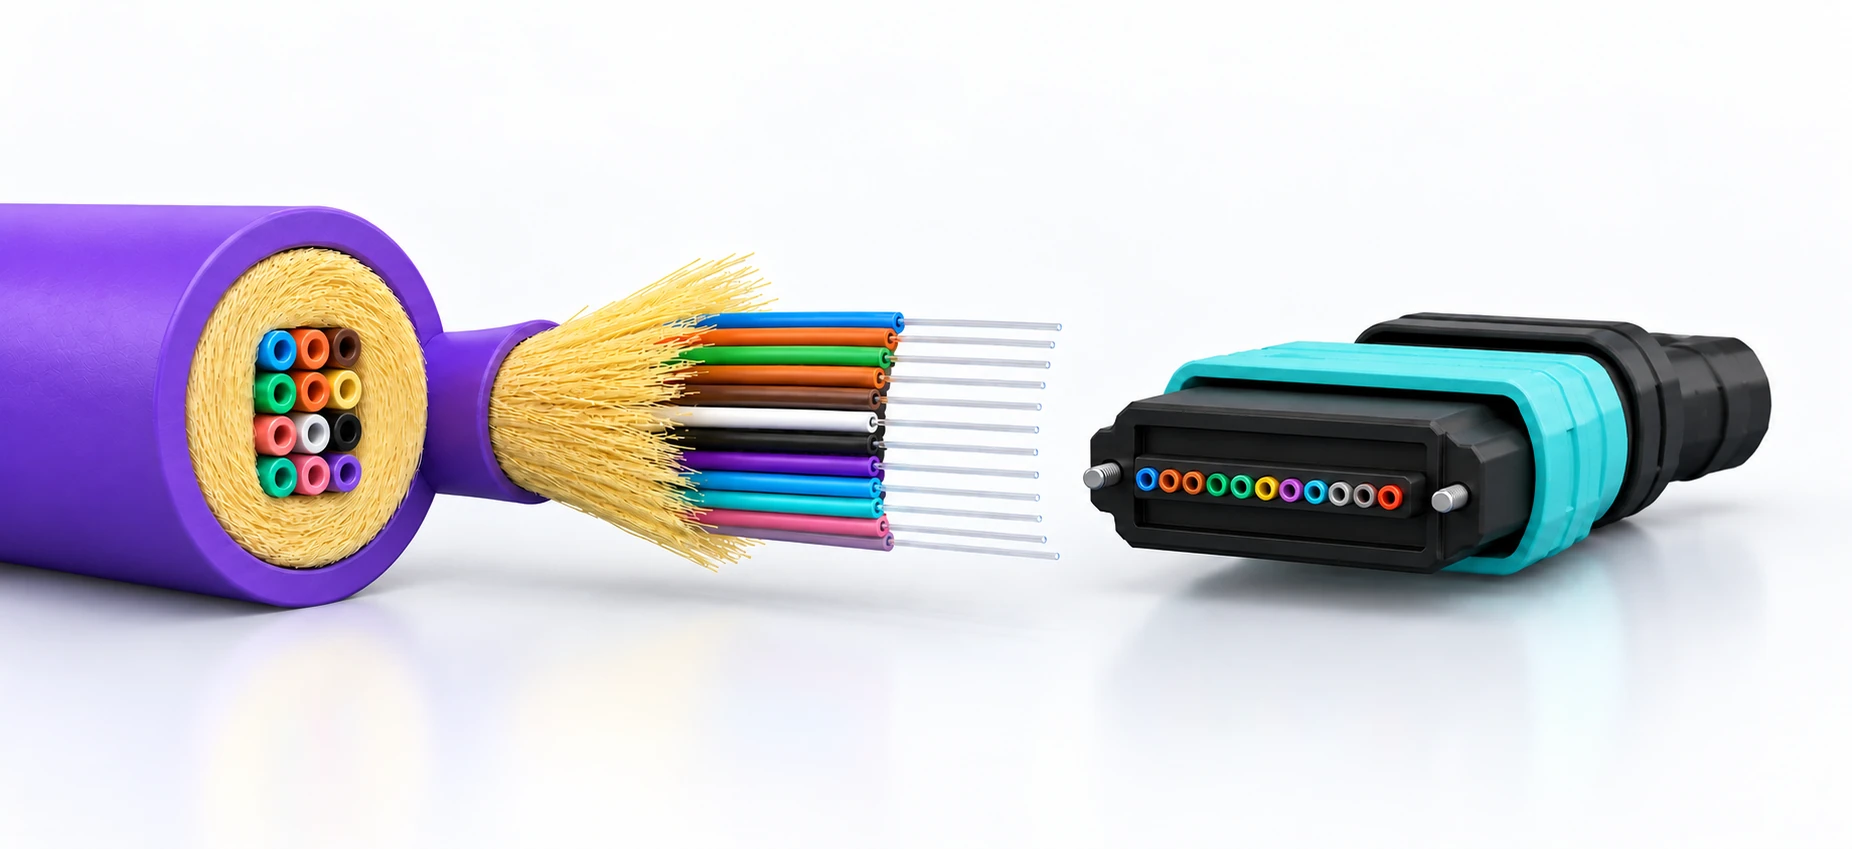
31 عملیات و نقاط کنترل در هفت مرحله. یک مرحله را برای مشاهده محدوده کامل آن باز کنید.
Before production: approve the launch assembly, cable drawing, fiber category and count, connector rows, gender, key orientation, polish, channel map and acceptance plan. The signed work instruction controls the exact sequence.
هویت فیبر، مشخصات، سازگاری پوشش، محمولههای مواد و خط پایه نوری ورودی را تأیید کنید.
پرداخت فیبر → آمادهسازی پیکربندیشده → اکستروژن بافر → خنککاری → نظارت ابعادی → کشش و پیچش. هر ردیف تمامشده را شناسایی کنید.
از نقشه کابل و ترتیب تغذیه تأییدشده پیروی کنید. این مرجع یک هسته بستهبندیشده تشکیل میدهد، نه یک نوار تخت. رابط قفسک جمعآوری را تأیید کنید.
بستههای نخ، راهنماها و کشش کنترلشده را با ساختار تأییدشده مطابقت دهید.
اکستروژن روکش مشترک → خنککاری → نظارت بر قطر → کپستان و پیچش. ردیف تمامشده را به لاتهای فیبر، نخ و پلیمر متصل کنید.
Verify construction, dimensions, identification, continuity and the agreed optical results against the cable control plan.
Scope tensile, crush, bend and temperature checks with the agreed methods and sampling plan. Cable-laboratory instruments are separate from online gauges and MPO testers.
Retain cable-stage acceptance records. Carry the source-reel identity into every measured and cut assembly length.
Cut to the approved assembly length and branch plan. Carry source-reel identity to each piece. This operation is required even without a separately quoted cutting machine.
Expose the specified fiber length and prepare the strength members without damage. Follow the cable and connector preparation instructions.
Place the specified boots and hardware on the cable in the connector-defined order before later operations prevent access. Verify the component set against the assembly BOM.
Use thermal stripping only with a compatible fiber/coating and approved instruction. Check stripped length and fiber damage.
Identify and place each fiber in its approved linear position. The arranger does not choose or create polarity.
Use a holder matched to fiber count, pitch and material. Recheck order after clamping and retain an identified array record.
Check the selected ferrule, adhesive, process liquids, shelf life, preparation and working time. The work instruction determines the adhesive-and-fiber loading sequence.
Use centrifugal degassing only when required by the material instruction. Link the batch, usable-life status and preparation cycle to the ferrules.
The quoted suction unit is not a universal filling method. Confirm its use, settings and verification with the connector and material instructions.
Confirm ferrule lot, orientation and loaded-array order. This is a required operation; the reference equipment list does not establish a separate powered loader.
Use the qualified adhesive recipe. Record holder, batch, load, time-temperature evidence and post-cure inspection. Oven quantity alone does not prove capacity.
Perform at the connector-defined point, which may differ from this overview order. Prove matched jaws and tooling with the actual housing and aramid arrangement.
Use the connector-approved preparation method and revision. Check the identified ferrule before it enters the polishing route.
Define the removal boundary and whether scraping is normal production or permitted rework. Keep before/after evidence and a damage check.
Match ferrule and polish geometry. The referenced 24-position fixture counts holding positions, not fibers or guaranteed output.
Control load, time, films, pads, cloths, liquids and the cleaning sequence. Retain recipe revision, consumable lots and permitted rework history.
Include only after confirming the processed object, liquid, timing and compatibility. It is not an automatic cleaning step for every MPO assembly.
Use the approved cleaning method and handling controls. Protect the finished surface and pass the identified assembly to inspection.
Use a qualified MPO adapter. Retain identified full-array images and the clean → re-inspect → disposition record. Visual inspection does not replace geometry or optical tests.
Apply the agreed attributes, limits and inspection plan. Retain raw reports, adapter/reference identity and repeatability evidence.
Check both ends against the signed channel map, gender and key orientation. The tester detects mapping errors; it does not correct them.
Match wavelengths, metrics, directions, references and limits to the product. The quoted system is a multimode reference; single-mode and return-loss needs require separate scope review.
Link the final assembly to its source reel, component lots and channel-level results. Fit protective caps and retain the release and packaging record.
Shell removal is rework only unless the connector instruction explicitly states otherwise. Confirm housing compatibility and use limits. After permitted reassembly or rework, repeat the required inspection, polarity and optical checks. Retain the original failed result as well as the repeat results.
03COMPLETE FACTORY FLOW
Separate manufacturing and assembly areas.
Clear release points. Connected production records.
Manufacture and release the MPO base cable.
Complete, test and release finished MPO assemblies.
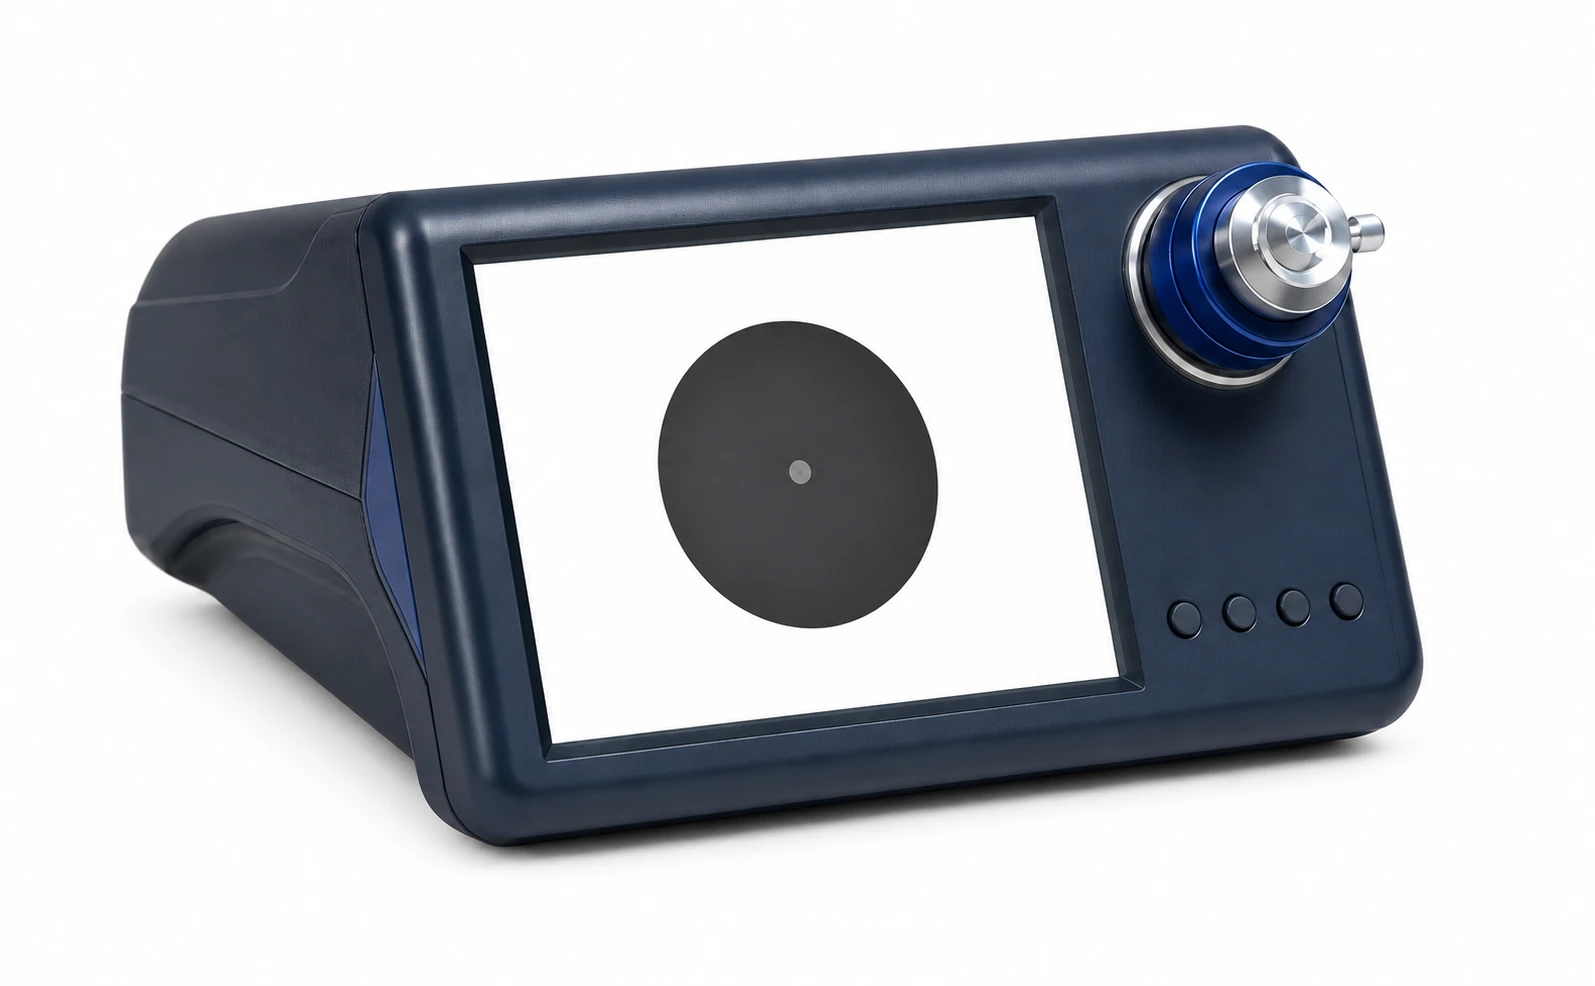
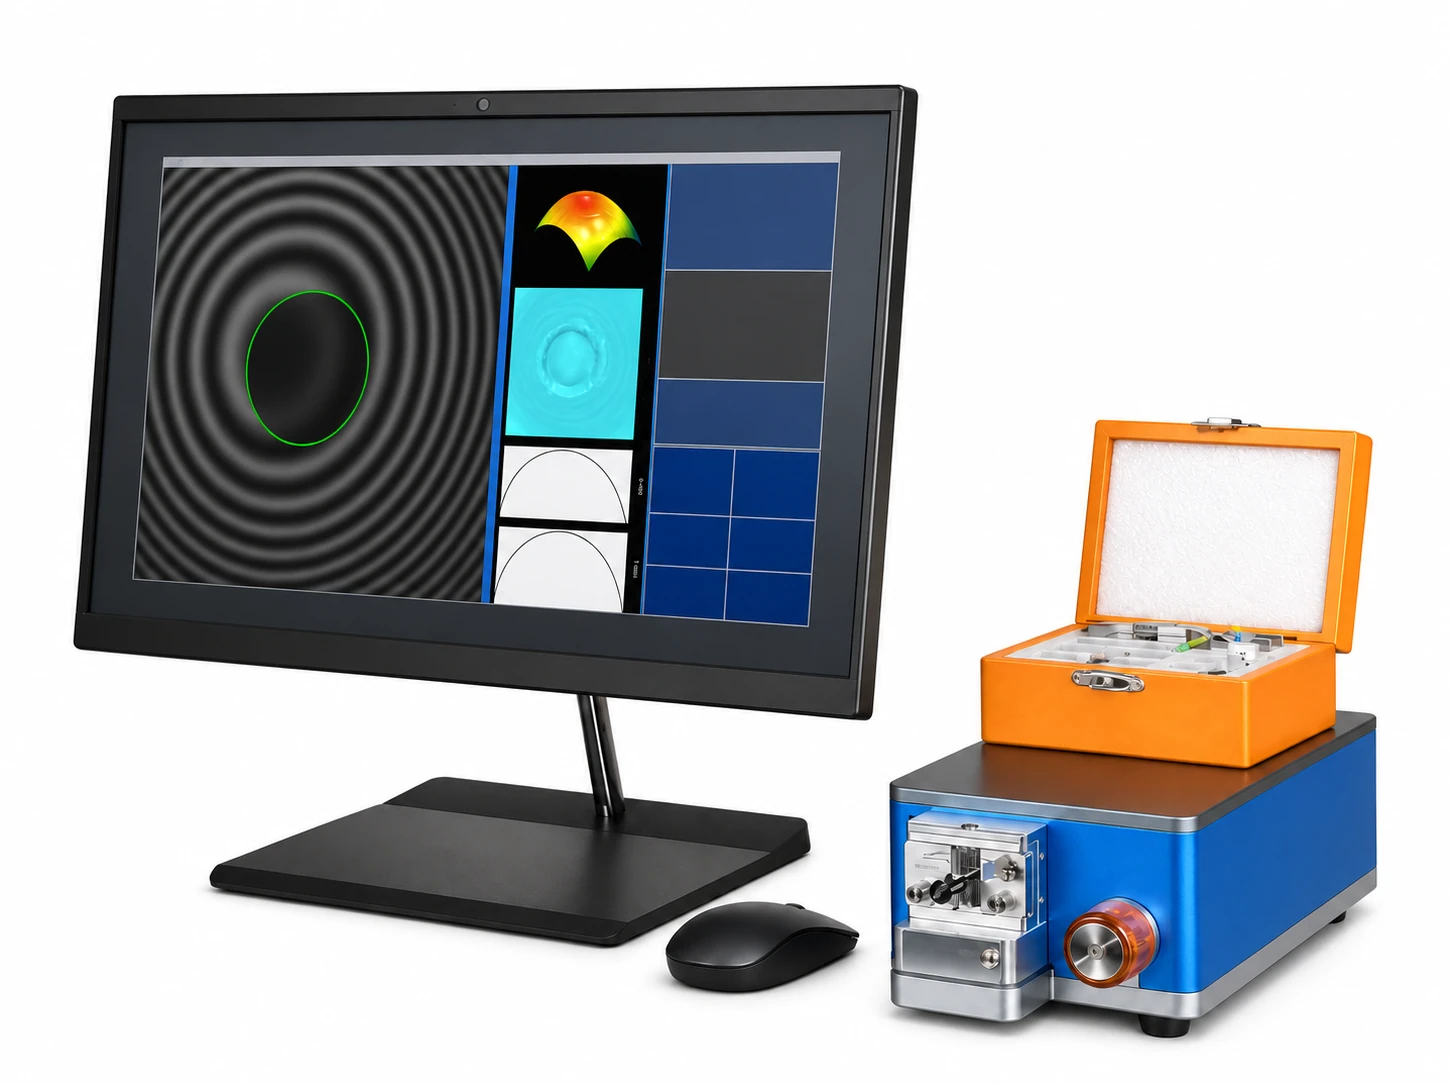
یک هویت مونتاژ. Keep the link from input fiber reel to finished cable reel, cut length, component lots, ferrule, cure and polishing recipe, inspection images and channel results.
Retain failed and reworked records. An optical pass does not replace the base cable’s own acceptance evidence.
04PROJECT REQUIREMENT SNAPSHOT
The first decision is your launch assembly. It defines the cable construction, connector workcells and evidence needed for release.
Build your project briefThe illustrated launch example is a 12-fiber GJFJV-type cable feeding MPO assembly. Other constructions require a matched route.
05EQUIPMENT BY PRODUCTION STAGE
خطوط کامل کابل، ابزارهای تخصصی مونتاژ و ابزارهای جداگانه رهاکننده.
یک خط کامل برای فیبرهای بافرشده بهصورت جداگانه: پرداخت، اکستروژن، خنککاری، کنترل ابعادی و جمعآوری. ماده فیبر، ماده بافر، ابزارها و روش رهاسازی را تأیید کنید.
An HK-50 reference configuration with matched fiber gathering, aramid handling, common-jacket extrusion, cooling and take-up. State whether the gathering cage is integrated or separately matched.
نام تجهیزات، صفحه خط تولید یا راهنمای فرآیند مربوط به آن تجهیز را باز میکند. برای مشاهده یادداشتهای مربوط به دامنه و پذیرش، یک تصویر را انتخاب کنید. “Launch route” refers to this reference product, not every MPO design. Equipment illustrations show a reference configuration. Confirm the final equipment scope for your project.
06RAW MATERIALS & INITIAL BOM SUPPORT
Plan the cable inputs, connector components and process consumables together, so the first production run has a complete material path.
درجهبندی مواد را با نقشه کابل و پنجره فرآیند مطابقت دهید قبل از اینکه اولین نوبت تولید را اندازهگیری کنید.
Explore cable materials
Fiber category, coating compatibility, reel identity and incoming checks.
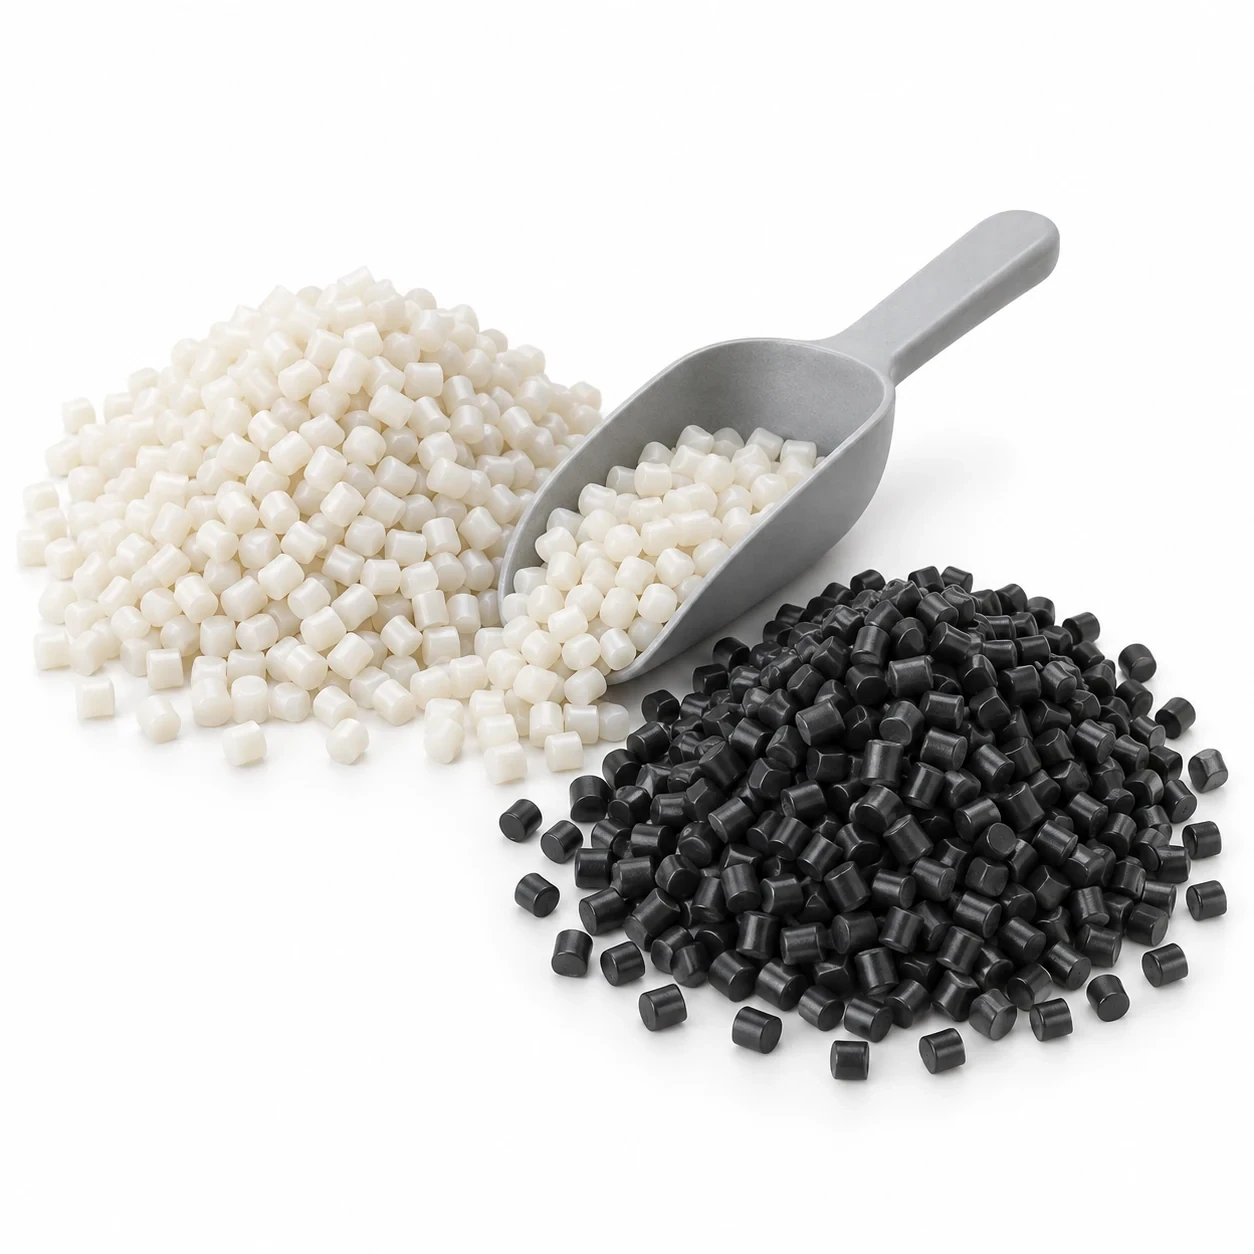
Separate tight-buffer and outer-jacket grades; agree processing and storage conditions.

Construction, linear density, tension range and package compatibility.
منابع مطالب تشریحی. قطعات دقیق، درجات و مصارف مطابق با محصول و فرآیند تأییدشده است.
Material specifications, supplier review, sample checks and an initial cable BOM.
07FACTORY LAYOUT & UTILITIES
جریان مواد را متصل کنید. کارهای سنگین ساخت کابل را از مونتاژ دقیق کانکتور جدا نمایید.
Plan machine lengths, service access, reel routes, lifting and safe aisles around the confirmed equipment.

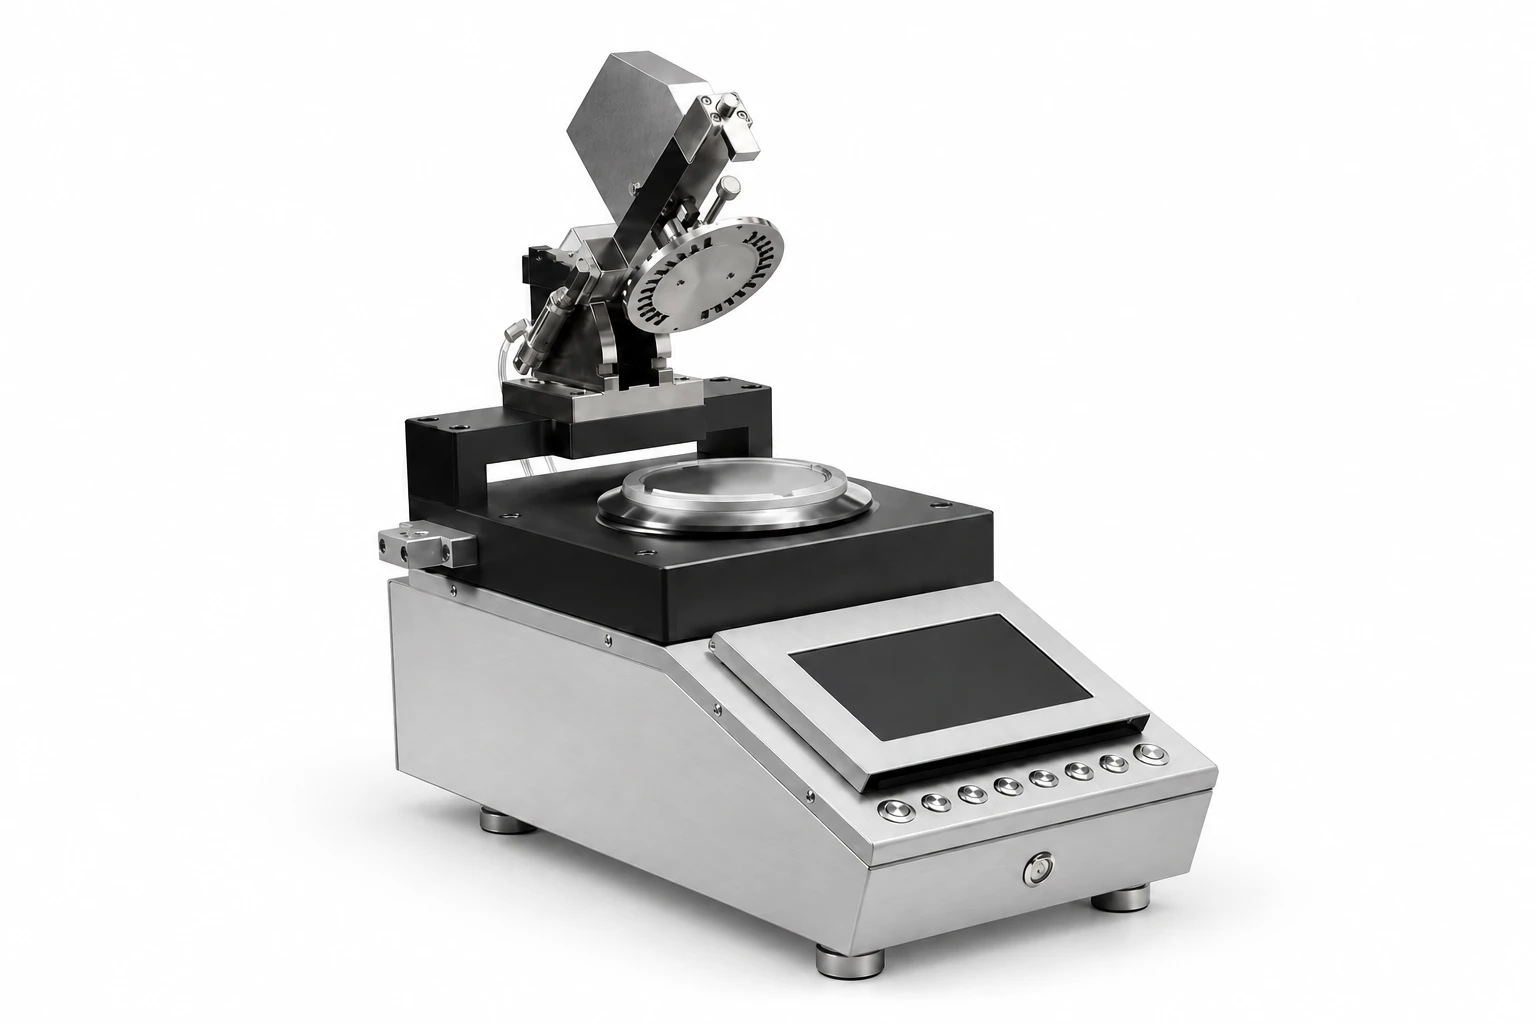
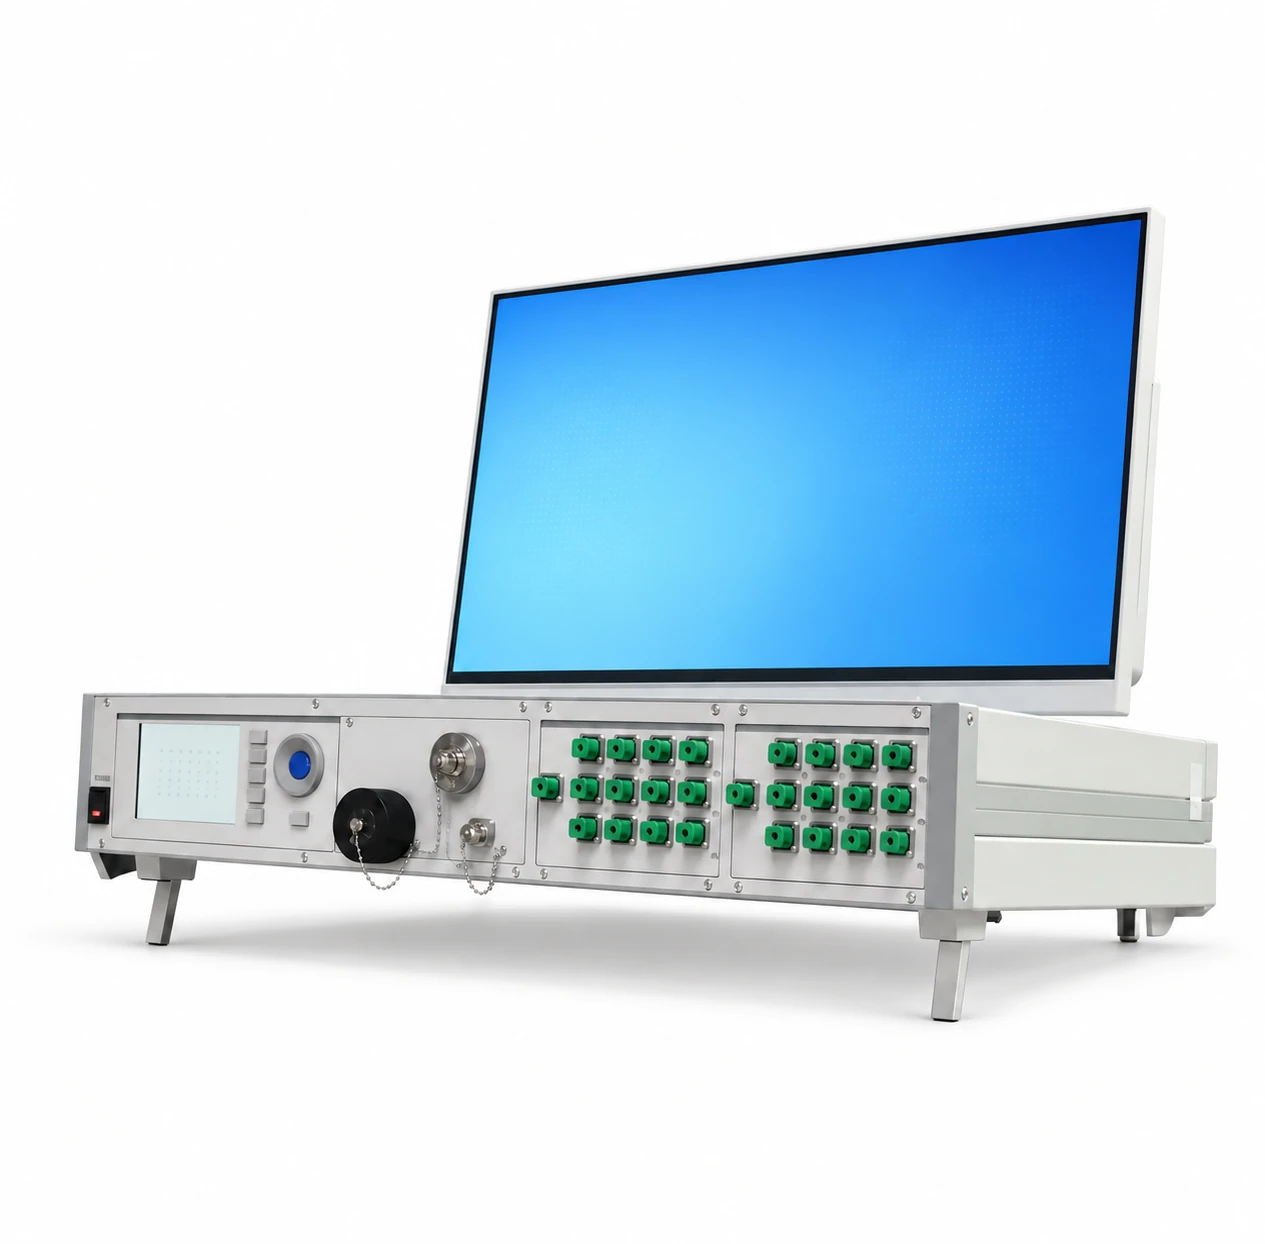
Define cleanliness, handling, ESD where applicable and storage conditions from the selected process. No generic cleanroom class is assumed.
ولتاژ، فرکانس، بارهای متصل و حفاظت.
Line cooling, water quality and recirculation.
هوای فشرده، تهویه و استخراج اختصاصی فرآیند.
ایستگاههای کاری، برچسبها، سوابق و ذخیرهسازی فایلهای نتایج.
طرح نهایی مطابق با ابعاد ساختمان شما، ماشینآلات انتخابشده و بررسی ایمنی تنظیم میشود. این مناطق گردش کار بهعنوان نقشهی ساخت محسوب نمیشوند.
08PHASED FACTORY CONFIGURATION
A complete factory can be planned in phases. Keep one approved launch product and a clear acceptance boundary at each step.
Plan cable manufacturing, cable release, MPO assembly and final testing as one coordinated project.
Best starting point for discussing a complete new factory.
Plan My MPO Factory09PROJECT SCOPE & RESPONSIBILITY
HONGKAI engineers the cable-making route and coordinates specialist MPO assembly, inspection and test equipment. The signed scope defines who supplies, proves and supports each part.
10EXECUTION, FAT & HANDOVER
Milestones are agreed after scope review. Each step has a decision and a deliverable, not a generic lead-time promise.
محصول را راهاندازی کنید، نقشه کانال، خروجی هدف و برنامه پذیرش را تعیین نمایید.
خطوط تطبیقدادهشده، سلولهای کاری، لیست مواد (BOM)، چیدمان و ماتریس مسئولیت.
Run the purchased route at FAT and retain the linked evidence.
Check site readiness, install and commission the defined scope.
اپراتورهای قطار را آموزش دهید، بررسیهای توافقشده را تکرار کنید و موارد باز را ببندید.
Follow one identified launch assembly from the source cable reel to its final channel results. Include cable-stage and back-end acceptance in the same project plan.
Read the complete process guideCable drawing, connector system, channel map and test limits.
Cable results, cure record, end-face images, geometry when specified and channel test files.
Repeatable work instructions, recipe control, cleaning, test setup and permitted rework.
درخواست یک اجرای نمونه توافقشده و بسته مدارک مربوط به حوزهای که خریداری میکنید را داشته باشید.
Images on this page are presentation references. They are not a claim that a specific customer factory has been delivered.
11KNOWLEDGE & DECISION SUPPORT
12FREQUENTLY ASKED QUESTIONS
Answers to the questions that change a project’s scope.
خیر. کارخانه مرجع، خطوط کامل تولید کابل را با سلولهای کاری مونتاژ و بازرسی دقیق MPO ترکیب میکند. کابل آزادشده بین این دو سیستم همراه با شناسه و سوابق پذیرش خود جابهجا میشود.
این محدوده با فیبر نوری خریداریشده آغاز میشود. تولید پیشفرم فیبر نوری و کشش فیبر در مسیر مرجع گنجانده نشدهاند.
در مرجع 12-فیبر نشاندادهشده در اینجا وجود ندارد. فیبرهای بافر شدهٔ جداگانه، هستهٔ کابل بستهبندیشده را تشکیل میدهند. آرایهٔ خطی فیبرها در طول آمادهسازی کانکتور MPO و بر اساس نقشهٔ کانال تأییدشده شکل میگیرد.
شماره دستهبندی فیبر و تعداد آن، ساختار کابل، ردیفهای فِرول، جنسیت (نری یا مادگی)، جهتگیری کلید، پولیش، قطبیت و الزامات آزمون، ماشینآلات، فیکسچرها و آداپتورهای سازگار را تعیین میکنند. گسترش را برای محصولات آینده نامبرده شده تأیید کنید.
هر دو بخشی از بحث دربارهٔ دامنه هستند و بهصورت خودکار گنجانده نمیشوند. لیست مواد (BOM) امضاشده و ماتریس مسئولیت، مواد تأمینشده، حمایت در تأمین، ابزارهای آزمایشگاه کابل، آزمونهای تخصصی مونتاژ و هرگونه موردی که توسط خریدار تأمین میشود را مشخص میکنند.
بله، این یک گزینه برنامهریزی است. با کابل خریداریشده واجد شرایط و مسیر توافقشده برای رهاسازی مونتاژ شروع کنید، سپس عملیات بافرینگ و روکش داخلی را به عنوان یک فاز گسترش جداگانه ارزیابی نمایید. ظرفیت و سازگاری همچنان نیازمند بررسی هستند.
MPO خانوادهی رابط کانکتور است. MTP® یک برند از شرکت US Conec برای کانکتور MPO است. مشخصات عمومی کارخانهی MPO، تأمین قطعات، مجوز یا سازگاری با اجزای MTP را تأیید نمیکند؛ در مستندات پروژه، سیستم کانکتور را بهصورت مشخص نامگذاری کنید.
Capacity, floor space and delivery time are confirmed from your launch-product mix, target output, shifts, validated cycle times, equipment arrangement, utilities and site readiness. The agreed configuration defines the project-specific figures.
13YOUR MPO FACTORY PROJECT
Build a project brief around your MPO product, production target and site. Leave undecided specifications open for engineering review.
Review your brief before sending it to HONGKAI. Nothing is sent automatically.
نقشه کابل، مشخصات کانکتور و طرح کارخانه شما. میتوانید اینها را در طی پیگیری فنی به اشتراک بگذارید.
 English English
 Русский
 हिन्दी
 한국어
 বাংলা
 Bahasa Indonesia
 Tiếng Việt
 മലയാളം
 Português do Brasil
 العربية
 فارسی