
A cable factory owner or production manager needs more than a video of a new production line running. Before accepting the equipment, agree on the trial cable, the required product quality, the supplied configuration and the evidence that will be kept. These decisions should be made before a factory acceptance test (FAT), then carried through to the site acceptance test (SAT) at the customer’s factory.
For a cable production line, FAT should demonstrate the agreed equipment configuration and selected trial products before shipment. SAT should verify installation, running behavior and product quality at the customer’s factory. Select the products and test conditions in advance, and close any failed acceptance item through a recorded correction and retest.
FAT and SAT are project-specific acceptance stages. IEC’s guidance for process-industry automation systems likewise emphasizes agreement on specifications, test scope and responsibilities; that is useful planning context, not a claim that every cable line is certified to that standard.1 نمونههای عملی خط کابل در زیر از تجربه تأییدشده راهاندازی HONGKAI استفاده میکنند و حدود آزمون واقعی به محصول و توافق خرید مشتری واگذار شده است.
محصولات آزمایشی را انتخاب کنید که سفارش را اثبات کنند
A supplier-factory FAT does not automatically cover every cable in the customer’s future catalogue. Agree on a manageable group of representative products: the cables expected to account for substantial production, together with a technically demanding construction that exercises the ordered equipment. Record what the trial leaves untested.
Testing every specification at the supplier’s workshop may require different material grades, incoming sizes, reels and tooling. The preparation and material consumption can be substantial. In the HONGKAI practice described for this guide, selection therefore starts with commercially important products and a few constructions that can meaningfully verify the equipment. A higher-element-count optical cable may be one such sample when it exercises the processes and quality requirements included in the order; a high core count alone does not prove every process capability.
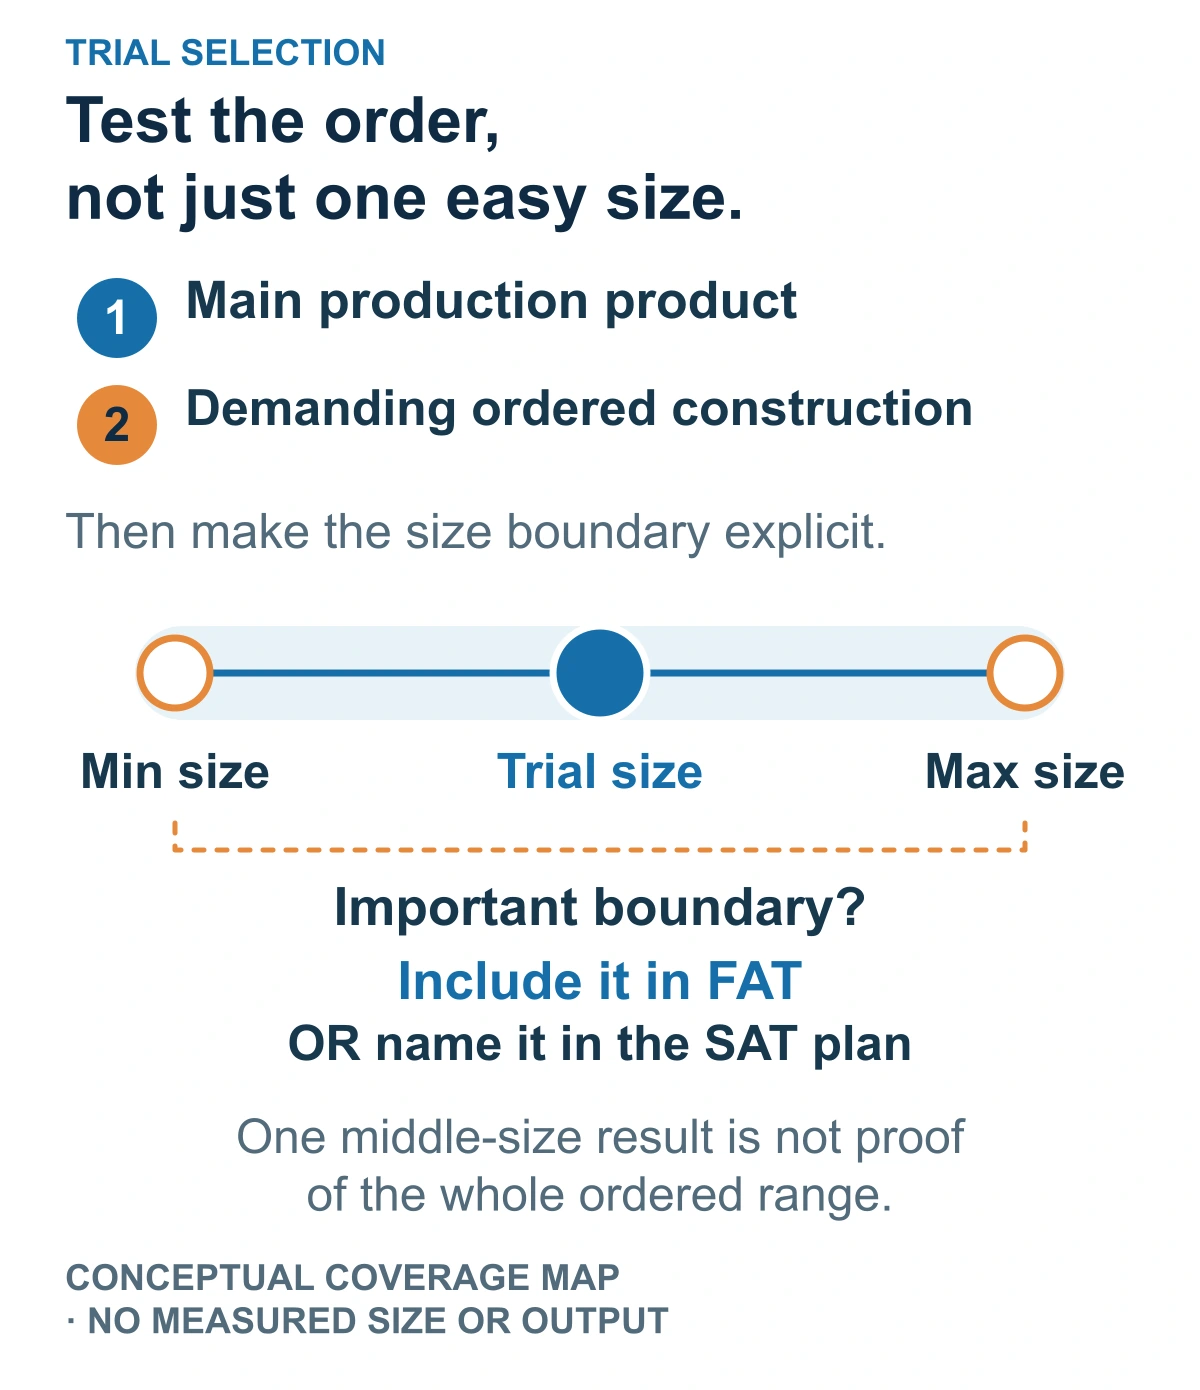
نقشه پوشش مفهومی: یک آزمایش موفق با اندازه متوسط، کل محدوده سفارشدادهشده را اثبات نمیکند. این یک ابزار کمکی برای انتخاب است، نه دادههای اندازهگیریشده محصول یا تولید.
Minimum and maximum sizes belong in the FAT plan when those boundaries are important to the purchase. Do not silently assume that one successful mid-range product proves both extremes. If a boundary is left for the customer’s site, name that product and its later verification step in the test matrix.
At the customer’s factory, plan to test each intended product or specification in the agreed commissioning range. Materials must be ready, and the trial quantity should reflect what is needed to evaluate the product without unnecessary waste. A large catalogue may need a staged schedule rather than one uninterrupted acceptance day.
| زمین آزمایش خط کابل | قبل از طراحی و آزمایش موافقت کنید | با نتیجه همراه باشید |
|---|---|---|
| Product identity | نقشه یا بازنگری نمونه، ساخت، ابعاد مورد نیاز و معیارهای کیفی | محصول دقیق ساختهشده و هر محدودهی آزمایشنشده |
| مواد | گرید، ابعاد ورودی و تأمینکننده/مشتری | مواد واقعی استفادهشده در آزمایش |
| رولها و نحوه جابجایی | ابعاد قرقره و سازگاری آن با تجهیزات پیشفاکتور شده | بسته واقعی پرداخت و دریافت |
| پیکربندی | ماشینآلات، ابزارها و محدوده کنترل/ابزار دقیق مرتبط | پیکربندی با سفارش بررسی شد |
| Running conditions | Product-specific speed, trial quantity or duration, and any special operating test | Actual conditions and measured result |
| Acceptance evidence | Measurements, sample identification, video and record owners | Pass/fail conclusion and outstanding items |
Confirm the customer’s cable specifications, required results and reel compatibility before equipment design. The cable production line RFQ guide explains how to establish those inputs before comparing configurations. If a trial input later changes, the buyer should require the difference to be listed beside the result and approved for the stated test scope. A result obtained on a different material or reel should not become an unexplained guarantee for the ordered production setup.
What to ask: Which products will be tested before shipment, which will be tested at the customer’s factory, and which drawing, material and reel does each result cover?
FAT: Prove the Quoted Scope Before Shipment
At the supplier’s workshop, FAT should connect equipment operation to an acceptable trial product. In HONGKAI’s confirmed practice, the central evidence comprises the produced samples, records of the run, confirmation that the line configuration matches the order, and retained operating video for later traceability. Write the expected deliverables into the agreement before the trial.
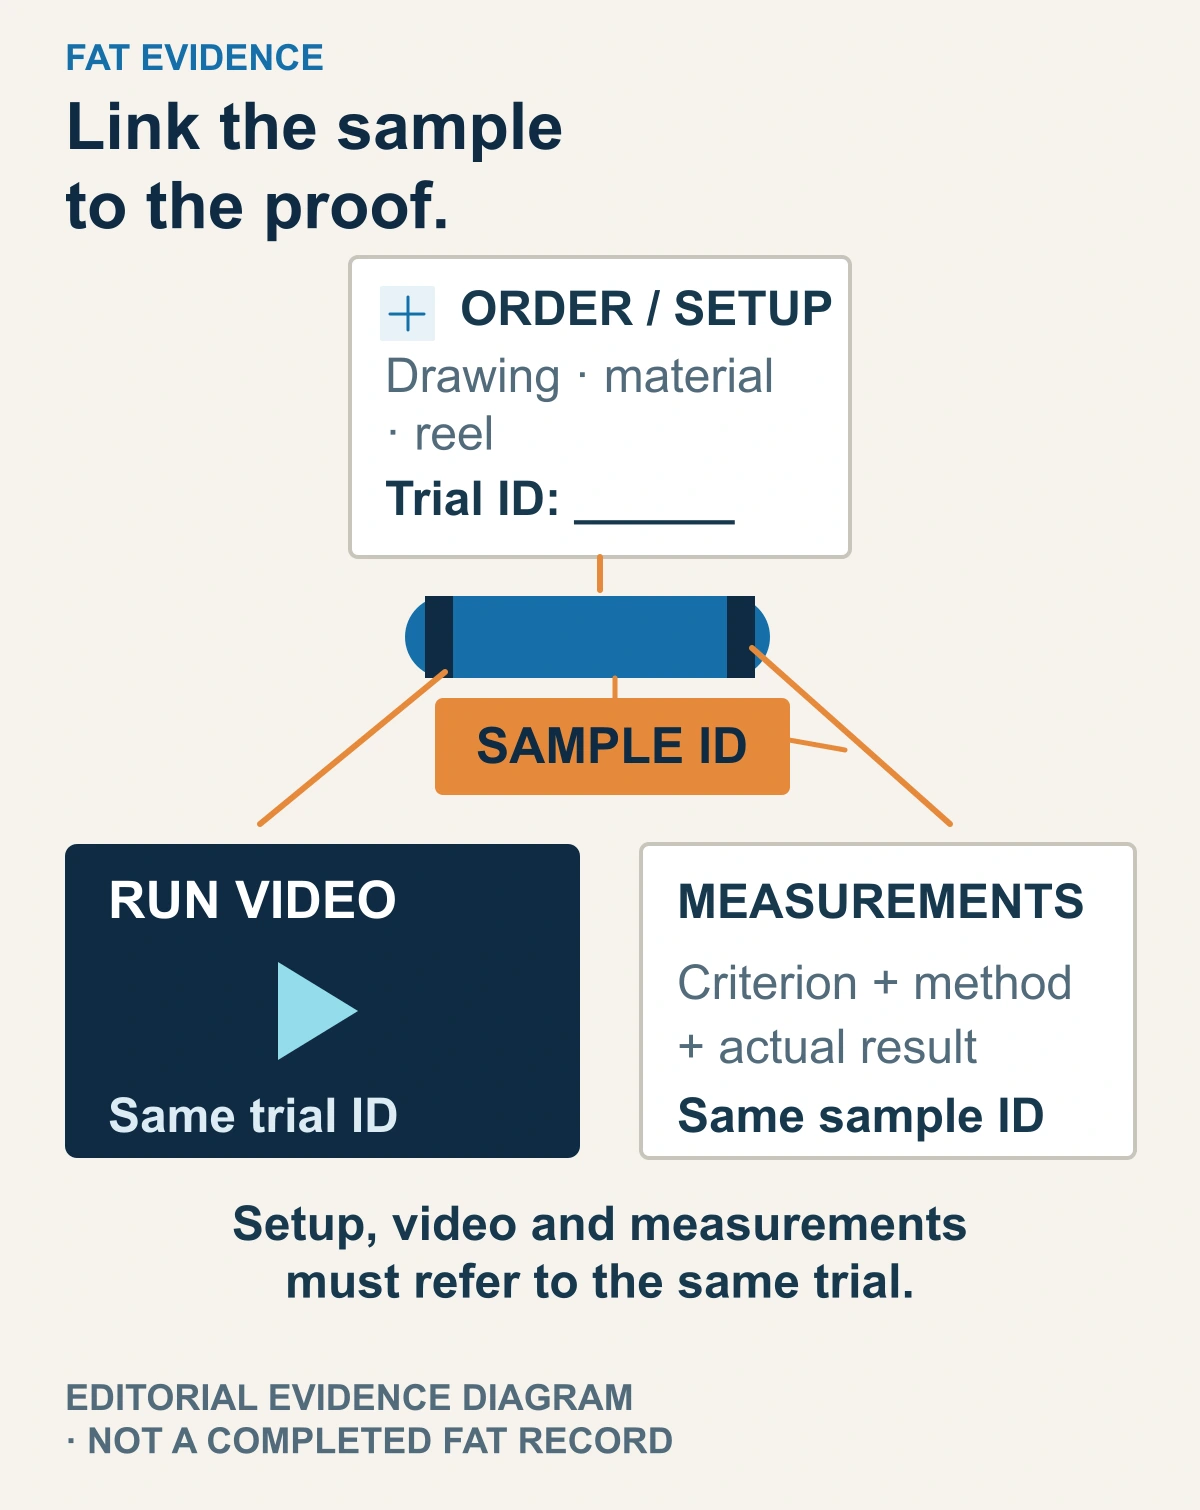
Editorial evidence diagram: link the actual sample, setup, run video and measurements to one trial. Blank identifiers are explanatory, not a completed FAT record.
A useful record starts with the machine configuration, product revision and trial inputs, then links the operating observations to the sample and its measured quality. Video can show the setup and running sequence; the relevant measurements establish whether the product meets its agreed criteria. For an insulation or sheath process, these may include centering, outside-diameter variation and surface condition. The crosshead tooling and centering guide explains why wall thickness and line setup need attention alongside outside diameter. Other cable structures need their own applicable checks.
| FAT deliverable | What the buyer should be able to establish |
|---|---|
| Identified samples | Which trial produced the retained sample, and which product revision does it represent? |
| Product measurements | Which agreed quality criteria passed, using which method or instrument? |
| Running record and video | What setup and operating conditions produced that sample? |
| Configuration comparison | آیا خط تأمینشده با محدوده سفارشدادهشده، از جمله قطعات و تجهیزات جانبی توافقشده، مطابقت دارد؟ |
| Open-item record | چه چیزی هنوز حلنشده باقی مانده، مالک اقدام کیست، و چه چیزی بستهشدن موضوع را نشان خواهد داد؟ |
Keep the sample identity consistent across the video, measurements and trial record. A video of one cable and a measurement sheet from another cannot establish the same result. Likewise, identify the processing stage: accepting a machine that produces a cable component does not establish the quality of downstream operations outside the supplied scope.
The routine FAT evidence package described here focuses on product results, operation and configuration. Define any additional protective-function demonstrations, safety documentation or other special tests separately in the project agreement; this matrix does not represent a complete machinery-safety assessment.
Evidence to request: A deliverables list agreed before FAT, followed by the identified sample results, configuration comparison, running record, video and open-item log for the actual trial.
SAT: خط نصبشده و رابطهای کارخانه را دوباره بررسی کنید
SAT means site acceptance testing after installation at the customer’s factory. For the cable line described here, verify that the equipment is fixed and aligned, runs properly during acceleration, steady operation and deceleration, and makes products that meet the agreed requirements. Prepare the customer’s utilities, materials and people before that trial.
In the commissioning scope described for this guide, the equipment supplier’s team handles equipment fixing, line leveling/alignment, operating checks and the production trial. The customer prepares the remaining site resources, including the power supply, cooling water and compressed air where needed, trial materials, operators and required measurement facilities. Confirm the exact division in the purchase and commissioning scope; do not infer that a supplier brings every resource needed at the customer’s factory. For an optical-cable project, the راهنمای نصب و راهاندازی خط فیبر توالی آمادگی سایت و تحویل را با جزئیات بیشتری توسعه میدهد.
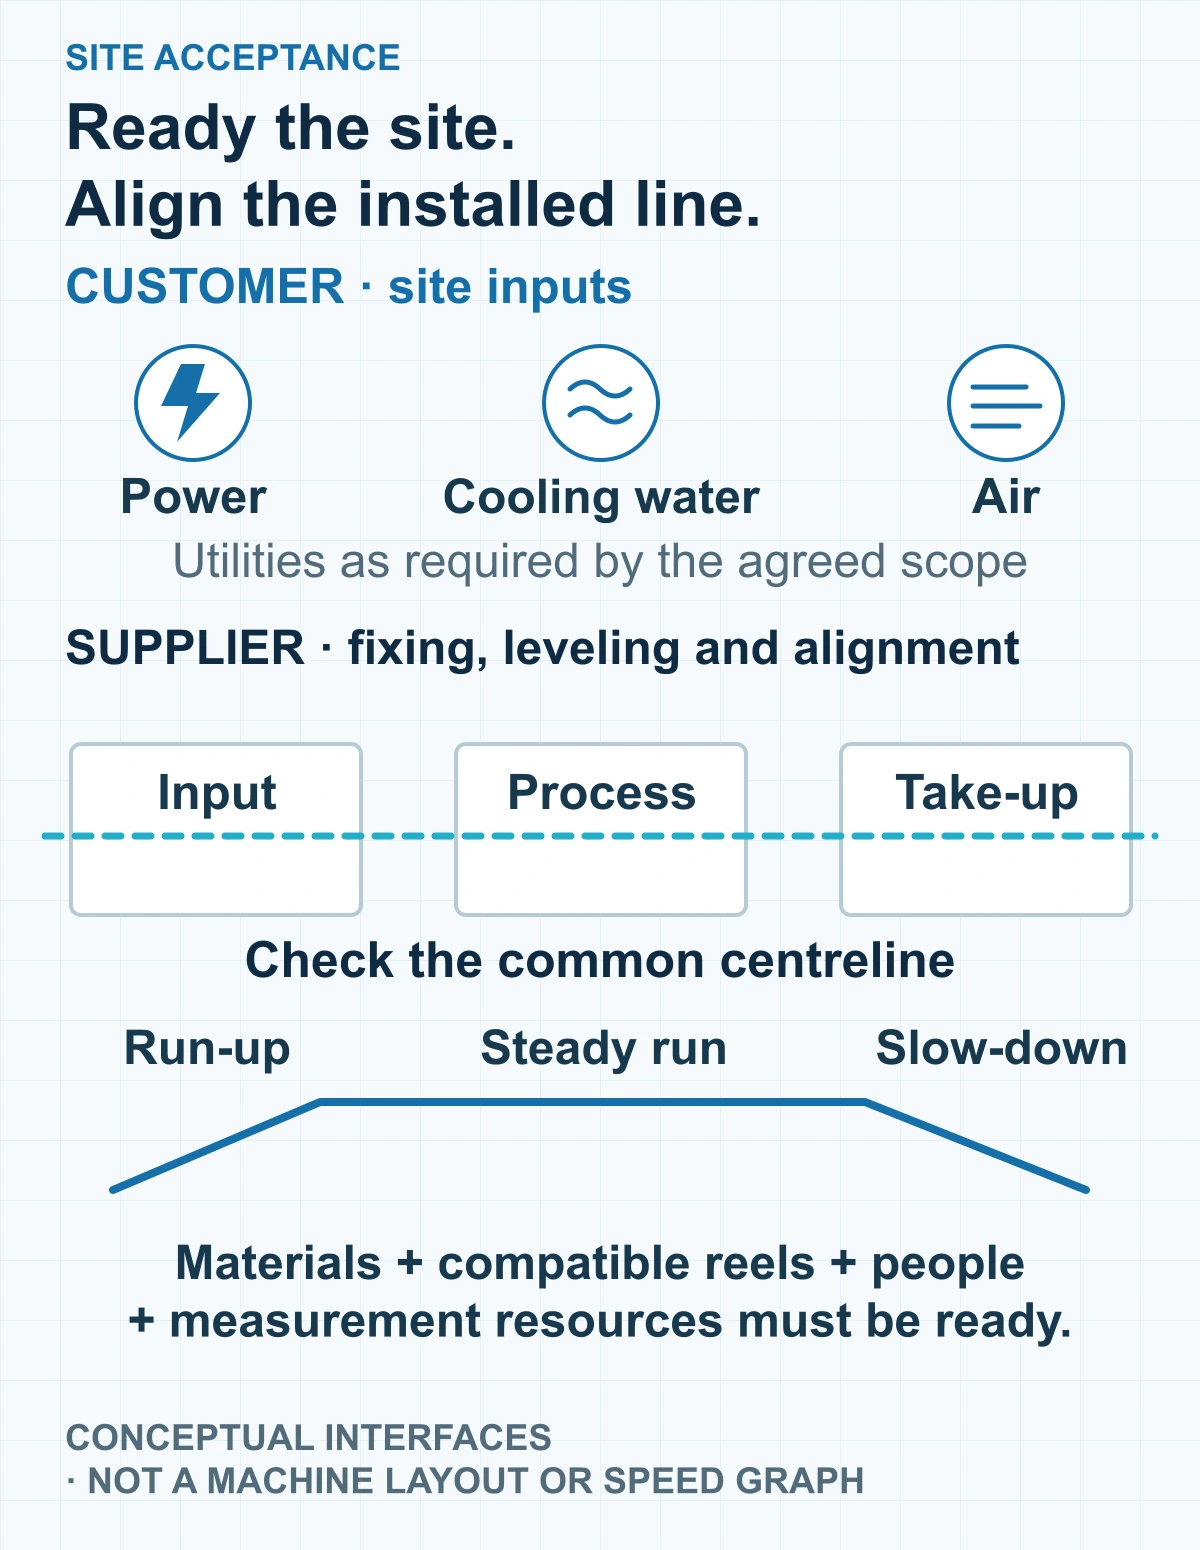
Conceptual site-interface diagram, not an equipment layout or measured speed graph. Confirm actual utilities, materials, reels, people and acceptance responsibilities in the project scope.
Use a site trial schedule that identifies each product, its inputs, quantity and acceptance measurements. If the materials, reels or connected equipment differ from FAT, record the differences. This gives both parties a basis for separating an installation problem, a changed input and an equipment defect when a result is unsatisfactory.
| وظیفه پذیرش محلی | مسئولیت در محدوده توصیفشده | مدارک برای موافقت و نگهداری |
|---|---|---|
| Ready the site | Customer | امکانات مورد نیاز در دسترس؛ مواد مناسب، قرقرهها، اپراتورها و منابع اندازهگیری آماده هستند |
| تعمیر و تنظیم تجهیزات | Supplier commissioning team, within agreed scope | Installation and line alignment checked |
| بررسی رفتار عملیاتی | تیم راهاندازی تأمینکننده | Acceleration, steady-running and deceleration observations |
| هر محصول آزمایشی را تأیید کنید | Supplier conducts trial; measurement and approval roles agreed | Identified samples and applicable product-quality results |
| Resolve deviations | Named person for each issue | Action, deadline and repeat-test result |
Agree on Useful Trial Quantities
As a HONGKAI commissioning-planning example, a customer may ask for one to two kilometres of each product. That is a project example, not a standard minimum. Agree on the needed length or duration in light of the product, the available raw material and the evidence required. The purpose is to obtain a meaningful product result without consuming material simply to extend the demonstration.
Normal stops and reel changes should be recorded where they affect the trial. Their role in acceptance depends on the agreed test, rather than an automatic failure rule. If a buyer needs to accept an automatic reel change, a particular restart sequence or another special operating function, specify that demonstration expressly.
A requested endurance run can also be agreed separately. Elapsed running time alone does not establish that the cable meets its quality requirements or that the entire equipment range has been verified. Preserve the relevant product results and operating conditions, whatever trial duration is chosen.
How to verify: For each product in the site plan, compare the measured result with its agreed specification, record the actual setup, and attach any deviation to the responsible person’s corrective action.
Close the Record Without Hiding Open Items
HONGKAI uses a project-management record to trace a test issue to the relevant personnel. The tester reports an issue or changed customer requirement, the responsible engineer carries out the correction within an assigned period, and testing personnel check the result again. The useful buyer question is whether this chain is visible for each open item.

Buyer decision diagram: record correction and retest or an explicitly agreed carry-forward decision. It is not an actual release approval or signed acceptance record.
| Acceptance issue field | چه چیزی را باید ثبت کرد |
|---|---|
| Finding | Product or equipment ID, trial conditions, failed criterion and supporting evidence |
| Required action | What must change; whether this is a defect correction or a requested scope revision |
| Responsibility | Assigned engineer or other responsible person, plus the record owner |
| Timing | Agreed correction deadline and planned retest date |
| Retest | Test conditions, measured result and reviewing personnel |
| تصمیم آزادسازی | Closed, held for retest, or expressly carried forward with an agreed owner and date |
Agree who has authority to approve acceptance and which items must close before shipment or site handover. If an item prevents the line from meeting an agreed product result, completing the promised configuration or conducting the required test, record the missing evidence and arrange correction and retesting before claiming that item has passed.
Some remaining work may be carried forward when both parties explicitly agree that it does not prevent the relevant release. The record still needs the item, responsible person, deadline and effect on shipment or site handover. Do not turn a requested design change into a quietly altered acceptance target; record the revision and its effect on the test plan.
Before closing FAT or SAT, assemble one connected package: the product and input schedule, ordered-versus-supplied configuration, identified samples, measured results, running records and video, and the corrective-action register. The buyer can then see which products have passed, which still need a trial, and which issues require a retest before the agreed next step.
-
IEC 62381:2024 — Automation systems in the process industry: FAT, SAT and SIT. The official scope describes project-specific acceptance specifications and agreement on test activities and responsibilities for automation systems. This article uses that planning principle only; it does not assert compliance or apply the standard as a universal cable-product acceptance specification. ↩
 English
 हिन्दी
 فارسی