


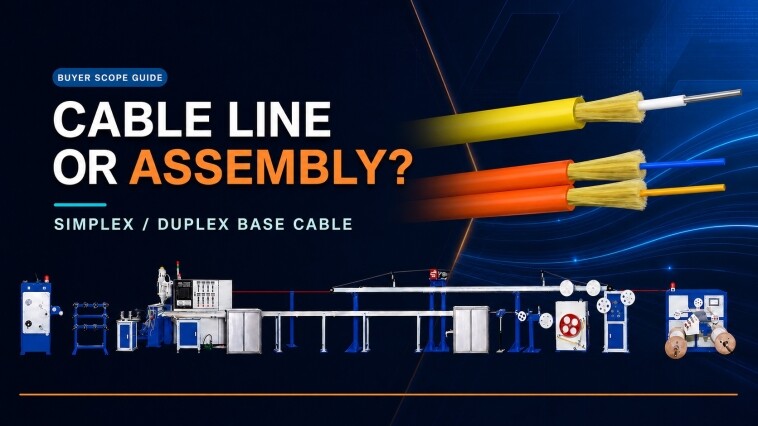
A fiber optic cable factory owner, production manager or technical buyer planning conventional patch cords must define two connected scopes. One scope makes the simplex or duplex base cable; the other cuts that cable and turns each end into an inspected, optically tested connector assembly.
A complete fiber optic patch-cord factory is not one extrusion line. It is either a qualified purchased-cable supply plus a complete connector-assembly workcell, or an integrated route that adds tight-buffer and outer-jacket production before the same back-end workcell.

Mapa de escopo do comprador: a linha de produção de cabos fabrica cabos base simplex ou duplex; a célula de trabalho separada de montagem de conectores transforma esse cabo em um patch cord LC ou SC acabado.
This guide maps the complete manufacturing boundary for conventional LC and SC patch cords. FC and ST may be added as project-specific fixture variants, but they are not the main production scope in this article. MPO and MTP multi-fiber assemblies are excluded because their cable construction, ferrule preparation, polishing, geometry control, polarity and multi-channel testing require a separate project scope.
O que inclui uma fábrica completa de cabos de manobra?
A complete patch-cord route must end with a saleable, traceable connectorized product—not merely a reel of cable or a visually polished connector. The proposal needs an owner and acceptance record for every stage from incoming fiber or cable through final optical test and packing.
| Manufacturing boundary | Entrada | Main output | Evidência antes da liberação |
|---|---|---|---|
| Produção de buffer apertado quando o cabo base é fabricado internamente | Composto de fibra óptica e tampão aprovado | Fibra com revestimento apertado qualificada | Identidade do material, dimensões, condição da superfície e verificação óptica acordada |
| Produção de aramida e revestimento externo quando o cabo base é fabricado internamente | Composto de fibra com buffer apertado aprovado, aramida e jaqueta | Cabo simplex ou duplex em um carretel | Desenho do cabo, dimensões, identificação da bobina, aparência e inspeção óptica acordada |
| Cable preparation | Carretel liberado ou cabo qualificado adquirido | Extremidades do cabo cortadas e preparadas | Comprimento, orientação, dimensões da tira e identidade do carrinho |
| Connector assembly | Cabo preparado, componentes do conector e consumíveis aprovados | Extremidades do conector montadas e curadas | Lote do componente, configurações do processo e registro de lote ou operador |
| Inspeção de polimento e face final | Conjunto de conector estabilizado | Limpe a face final da bucha | Processo de polimento aprovado e resultado da inspeção armazenado ou rastreável |
| Teste e acabamento ópticos | Patch cord concluído | Produto vendável liberado | Configuração do teste, comprimento de onda, resultados, identidade, etiqueta e registro de embalagem |
O Linha de produção de patch-cord HONGKAI supports the base-cable side for applicable constructions. The confirmed project route then adds partner-integrated back-end stations, together with connector-specific fixtures, hand tools and consumables. HONGKAI’s published modelo de fabricação e integração especializada explains this source boundary; the final commercial proposal must still distinguish HONGKAI-manufactured equipment, partner-integrated equipment and buyer-supplied items.
Common mistakes: A quotation calls the cable line a complete patch-cord factory but omits connectorization and optical testing. Another quotation lists a polishing machine but omits its connector fixtures, films, inspection adapter, reference cords or process responsibility.
Which HONGKAI Lines Make the Base Cable?
For the reviewed simplex or duplex construction, the HONGKAI route uses the HK-30 to produce tight-buffered fiber and the HK-50 to apply aramid reinforcement and the outer jacket. If the factory purchases qualified tight-buffered fiber, the cable-making scope can start with the HK-50.
HK-30 tight-buffer stage
The reviewed HK-30 configuration receives optical fiber and applies the specified tight-buffer layer. Its functional modules include controlled payoff, preheating, material drying and feeding, extrusion, warm and cold cooling, online diameter measurement, capstan control and take-up. These functions define the production stage; the customer’s approved construction must define the actual polymer, color, dimensions, reel format and acceptance limits.
Verified HONGKAI HK-30 3D reference showing the complete tight-buffer production line. Final tooling, material and operating values remain project-specific.
HK-50 aramid-and-jacket stage
The reviewed HK-50 configuration receives the approved tight-buffered input, pays off the aramid reinforcement and extrudes the outer jacket. Its functional modules include input payoff, adjustable aramid payoff, positioning, material preparation, extrusion, cooling, online diameter measurement, capstan, accumulation and take-up.

Verified HONGKAI HK-50 3D reference showing the complete line used for an applicable aramid-reinforced simplex or duplex jacket stage. The accepted cable construction controls the final configuration.
The complete in-house route is therefore HK-30 tight buffering followed by HK-50 aramid reinforcement and jacketing. An HK-50-only route is appropriate when the factory has an approved external source for tight-buffered fiber and the incoming package, material, dimensions and optical condition match the signed HK-50 input specification.
The HK-30 and HK-50 documents are older project configurations. They verify the process stages and equipment functions, but their speeds, tensions, power, output, material options and package sizes must not be copied into a new proposal without reconfirmation.
The earlier HONGKAI patch-cord cable process walkthrough also shows the HK-30 and HK-50 as separate production stages. Use it as orientation only; the approved cable drawing and current technical agreement control a new project.
How to verify: During FAT, connect the raw-fiber or tight-buffer input to the approved recipe and identify the resulting reel. Retain the actual cable drawing, material lots, tooling, dimensions, surface result, optical check and take-up package used for the trial.
Qual é o processo completo de back-end para um cabo de derivação LC ou SC?
The supplied conventional LC/SC package covers cable cutting, jacket and buffer stripping, adhesive preparation and dispensing, connector assembly, crimping, curing, fiber scribing, polishing, end-face inspection, optical testing, labeling and packing. The ten powered back-end stations are integrated through HONGKAI’s specialist partner; connector-specific hand tools, fixtures and consumables complete the route.
The sequence below is a controlled planning route for the supplied epoxy-and-polish package. It is not a universal connector recipe. The approved connector-component instructions must set the exact strip dimensions, cleaning method, adhesive, assembly order, crimp tooling, cure cycle, polish sequence and optical limits. A factory should turn those instructions into a traveler or batch record before FAT.
1. Release the incoming cable and production order
Before cutting, verify the cable drawing, connector family, ferrule finish, finished length, quantity, label data and test requirements. Record the incoming reel or cable lot against the work order. If base cable is made in house, the released HK-50 reel is the handoff point; if it is purchased, the supplier’s reel identity and incoming inspection are the handoff evidence.
Como verificar: O operador deve ser capaz de rastrear cada amostra FAT até um carretel de cabo aprovado, um lote de componente de conector e uma revisão da instrução de trabalho.
2. Cut the cable to controlled length
The automatic fiber cable cutting machine measures and cuts the released cable for the planned patch-cord length. The RFQ should define the cable-size range, required length range, tolerance, quantity count and whether allowance for stripping and connector assembly is included in the cutting instruction.
3D technical model based on the verified automatic cable cutting machine in Peter’s supplied conventional patch-cord package. Supplier branding has been removed; this back-end station is integrated through HONGKAI’s specialist partner.
Armadilha: Não aceite apenas o comprimento de corte exibido. Durante o FAT, meça uma amostra definida e mantenha tanto o valor ajustado quanto os resultados reais.
3. Strip the outer jacket
The optical cable stripping machine removes the required jacket length so the aramid yarn and buffered fiber can be prepared for the connector. The work instruction must match the actual simplex or duplex cable diameter, jacket material and connector boot or crimp sleeve. Acceptance should cover strip length, a clean cut and no damage to the reinforcement or buffered fiber.
3D technical model based on the verified outer-jacket stripping station. Supplier branding has been removed; final tooling is selected against the approved cable and connector construction.
4. Strip the tight buffer
The buffer stripping machine exposes the glass fiber to the dimension required by the connector assembly process. The operator must control the strip length and inspect the exposed fiber for coating residue, scratches or breakage. The machine does not replace cleaning and handling discipline.
3D technical model based on the verified tight-buffer stripping station in the supplied LC/SC package. Supplier branding has been removed.
O que perguntar: Solicite a gama aceitável de cabo e buffer, lista de lâminas ou ferramentas de reposição, método de verificação do comprimento de descascamento e critérios de rejeição para fibra danificada.
5. Prepare adhesive with the Model 800 centrifuge
For the reviewed epoxy-and-polish route, the approved adhesive is prepared according to its supplier instruction. The Model 800 epoxy centrifuge supports controlled preparation and removal of entrained air before dispensing. Adhesive identity, mix ratio when applicable, preparation time, usable life, storage condition and disposal rule belong in the batch record.
3D technical model based on the verified epoxy centrifuge in the supplied package. Supplier markings have been removed; the approved connector and adhesive suppliers—not the image—define the preparation recipe.
Armadilha: Uma lista de máquinas que mencione apenas “epóxi” deixa o comprador sem um sistema adesivo compatível, controle de lote ou regra de vida útil utilizável.
6. Dispense the adhesive
The epoxy dispenser delivers the prepared adhesive to the connector assembly process. The dispensing needle or adapter, dose, cleaning interval and confirmation method must suit the selected LC or SC connector components. Record the adhesive batch and preparation time with the work order.
3D technical model based on the verified adhesive dispensing station in the supplied conventional connector route. Supplier branding has been removed.
7. Insert the fiber, assemble components and crimp
The operator threads the prepared fiber into the ferrule, seats the cable and assembles the boot, crimp sleeve and other specified parts in the connector supplier’s approved order. The pneumatic crimping machine applies the connector-specific crimp through the correct die or fixture. The factory must provide stable compressed air at the agreed pressure and quality.
3D technical model based on the verified pneumatic crimping machine. Supplier branding has been removed; the connector construction controls the die, crimp position and acceptance check.
How to verify: Inspect component seating, aramid capture, boot position and crimp condition on representative LC and SC assemblies. Record the die or fixture identity and compressed-air condition used for FAT.
8. Cure a montagem do conector
The curing oven stabilizes the adhesive under the approved time-and-temperature instruction. The work instruction must define loading orientation, fixture or holder, setpoint, actual cycle evidence, batch size and handling after cure. Do not transfer a cure recipe from another adhesive or connector system without approval.
3D technical model based on the verified connector curing unit in the supplied LC/SC package. Supplier branding has been removed.
Evidência a solicitar: Um documento de FAT deve vincular cada amostra ao lote do adesivo, à identificação do forno, ao registro do ciclo e ao operador responsável.
9. Scribe excess fiber and prepare the ferrule for polishing
After the approved cure and cooling sequence, use the specified fiber cutting pen or scribing tool to remove the protruding fiber without chipping the ferrule or damaging the fiber. Clean the connector and polishing fixture before loading. This is a hand-tool step in the supplied package, not a reason to invent another machine.
Erros comuns: força excessiva durante a marcação, detritos transportados para o suporte de polimento e ausência de regra de substituição para ferramentas manuais desgastadas.
10. Polish the LC and SC ferrules
The fiber connector polishing machine performs the mechanical polishing stage. A complete station also needs the correct LC or SC holder, the approved UPC or APC process where applicable, polishing pads and films, cleaning materials and a controlled film-change rule. Peter’s supplied package lists connector-specific fixtures; they must be scheduled by actual launch product rather than assumed from the machine name.
3D technical model based on the verified polishing machine in the supplied package. Supplier branding has been removed; LC and SC require the correct connector-specific holder and approved consumable sequence.
What to ask: Require a connector-to-fixture matrix, film sequence, cleaning step, process ownership and replacement plan. A polishing machine without the right holder and consumables is not a working LC/SC station.
11. Clean and inspect the end face
After polishing, clean the connector with the approved materials and inspect it using the fiber connector inspection microscope with the correct adapter. The acceptance record should distinguish contamination that can be cleaned from scratches, chips or other defects that require rework or rejection.
3D technical model based on the verified ferrule inspection microscope in the supplied LC/SC workcell. Supplier branding has been removed.
IEC 61300-3-35:2022 covers visual inspection and classification of contamination, scratches and defects on fibre-optic connector interfaces. The product specification still needs to identify the applicable connector interface, inspection method and acceptance criteria. Visual inspection does not replace finished-product optical testing.
12. Measure insertion loss and return loss with the 7420B
The 7420B insertion-loss and return-loss tester is the final powered test station in the supplied package. Before FAT, define fiber type, wavelength, reference method, connector adapters, reference cords, test direction, acceptance limits, calibration responsibility and how each result is tied to the finished patch cord.
3D technical model based on the verified optical tester in the supplied package. Supplier branding has been removed; the station supports traceable insertion-loss and return-loss testing of the finished conventional patch cord.
IEC 61300-3-4:2023 aborda métodos de medição de atenuação, enquanto IEC 61300-3-6:2008 addresses return-loss measurement procedures. These references do not supply the product’s pass/fail values; those values must come from the approved product specification and customer agreement.
13. Perform final visual checks, label and pack
Use the visual fault locator when it belongs to the agreed work instruction, complete the final visual and dimensional checks, fit clean dust caps, apply the traceable label and pack the patch cord so the connector end faces and cable bend condition are protected. The released sample should carry the product code, length, connector configuration, fiber or cable identity, batch or serial reference and test status required by the buyer’s system.
The connector-processing area should be clean and have little airborne dust; a cleanroom is preferable when the product and quality requirements justify it. The layout must separate dirty preparation work from cleaned ferrules and finished connectors. The RFQ should assign compressed air, benches, lighting, cleaning materials, waste handling, labels and packaging instead of assuming they are included with the machines.
Pitfalls: The workcell depends on operator memory for strip length or polishing steps, end-face images are not tied to product identity, optical results have no documented reference method, or tested connectors are exposed to dust again before capping and packing.
Resumo dos equipamentos de back-end
| Process stage | Reference equipment | Controle adjacente necessário |
|---|---|---|
| Length cutting | Máquina automática de corte de cabos | Tolerância de comprimento, margem de erro e medição da amostra |
| Jacket stripping | Máquina de decapagem de cabo óptico | Ferramentas específicas para cabos e critérios de dano |
| Buffer stripping | Máquina de decapagem com buffer apertado | Inspeção e limpeza do estado da fibra |
| Adhesive preparation | Model 800 | Registro de identidade do adesivo, mistura e vida útil |
| Adhesive dispensing | Epoxy dispenser | Controle de dose, adaptador e limpeza |
| Connector crimping | Máquina pneumática de prensamento | Matriz específica do conector e ar comprimido |
| Curing | Forno de cura para conectores | Rastreabilidade aprovada de ciclo e lote |
| Ferrule polishing | Máquina de polimento de conectores de fibra | Fixação LC/SC, películas e sequência de limpeza |
| Inspeção da face final | Microscópio de inspeção de conector de fibra | Adaptador, critérios e resultado rastreável |
| Optical testing | 7420B | Comprimento de onda, configuração de referência, limites e calibração |
Which Fixtures, Tools and Consumables Belong in the RFQ?
Fixtures and consumables are part of the manufacturing system because they determine which connectors can be processed and whether the result is repeatable. A machine without the correct holder, film, adapter or cleaning control is not a complete station.
Peter’s supplied package names LC and SC polishing fixtures, including UPC and APC variants where applicable. FC and ST fixtures are also available in the reference package, but they should be added only when those connector families belong to the approved product list. The package also includes fiber and cable strippers, crimping pliers, aramid scissors, a fiber cutting pen, an electronic balance, adhesive, polishing pads and films, a visual fault locator and cleaning paper.
| Scope group | Itens a agendar | Decisão do comprador |
|---|---|---|
| Connector fixtures | Porta-polidores, adaptadores de inspeção, adaptadores de teste e qualquer fixação para prensagem ou montagem | Liste todas as famílias de conectores, acabamentos de férula e fornecedores de componentes |
| Ferramentas manuais de preparação | Decapador de fibra, decapador de jaqueta, tesoura para aramida, ferramenta de corte e alicate de crimpagem | Definir quantidade de substituição, alocação do operador e método de inspeção |
| Adhesive controls | Adesivo, ferramentas de pesagem ou mistura, centrífuga, dosador e materiais de limpeza | Congele o sistema adesivo compatível e os controles de armazenamento, preparação e vida útil |
| Polishing consumables | Almofadas, filmes e materiais de limpeza | Aprovar a sequência, grau, fornecedor, regra de alteração e controle de lote |
| Test accessories | Cabos de referência, adaptadores, mandris ou itens de condicionamento de modo, quando necessário, e localizador visual de falhas | Defina o método de teste, as interfaces dos conectores e a responsabilidade pela calibração |
| Finishing materials | Tampas de proteção contra poeira, etiquetas e materiais de embalagem | Definir limpeza, identidade, apresentação e proteção para expedição |
What to ask: Require a connector-to-fixture matrix and a consumable list for the launch products. The supplier should state which items are included, which wear out, which require regular replacement and which must be sourced from the connector or consumable manufacturer.
Uma nova fábrica deve comprar cabo base ou fabricá-lo internamente?
Start with the narrowest complete route that can release the intended saleable patch cord. Buying qualified cable concentrates investment and training on connector assembly; adding HK-30 and HK-50 brings cable construction and supply control in house but also adds extrusion, material, reel and intermediate-quality responsibilities. The broader mapa da rota de produção de cabos de fibra óptica ajuda os compradores a posicionar esta rota estreita de cabo interno ao lado de outras famílias de linhas de cabos ópticos sem tratar uma lista de máquinas como universal.
| Decision factor | Compre cabo base qualificado | Adicionar produção interna de cabos-base |
|---|---|---|
| Initial process scope | Qualificação do cabo de entrada mais montagem do conector | Processamento de tampão apertado, aramida e revestimento externo, além de montagem de conectores |
| Controle do fornecedor principal | Cable drawing, reel records and change notification | Fiber, compounds, tooling, recipes, in-process cable and reel traceability |
| Habilidades a desenvolver | Preparação, conectorização, polimento, inspeção e teste óptico | All assembly skills plus extrusion, cooling, tension and take-up control |
| Expansion constraint | Approved supplier portfolio and lead-time conditions | Janela de equipamento verificada, ferramental, material e plano de troca |
| Handoff risk | Incoming reel approval to the assembly traveler | HK-30 output to HK-50, then finished reel to connector assembly |
Decision criterion: Compare the approved product mix, cable-source reliability, process knowledge, staffing, quality system and traceability burden. Do not justify the integrated route only with an unsupported production-volume or payback threshold.
Red flags: A proposal adds cable extrusion without an intermediate-reel release plan, or assumes that owning the cable line automatically reduces finished-patch-cord defects. Control improves only when materials, work instructions, operators and evidence are qualified together.
Por que o MPO está excluído desta rota de equipamento?
MPO is excluded because both its incoming multi-fiber cable and its connector-assembly workcell can differ from conventional single-fiber patch cords. A polishing fixture alone does not convert the ordinary patch-cord route into an MPO route.
The supplied specialist catalog separates the ordinary patch-cord machines from a dedicated MPO/MTP group. That group includes multi-fiber-specific preparation, polishing fixtures, curing, end-face or geometry inspection, polarity or channel control and multi-channel optical testing. Peter’s supplied experience also identifies more stable automatic polishing pressure as an important MPO consideration because one connector presents multiple fibers to the polishing process.
This article therefore stops at conventional single-fiber connector families. A separate MPO article must begin with the exact cable construction, fiber count, ferrule and connector system, polarity, end-face geometry requirement and channel-test method before selecting equipment.
Note: The supplied conversation mentions a project range of multiple fibers per MPO connector. That range remains a bounded project observation and will not be published as a universal MPO specification without Peter’s confirmation.
O que o RFQ e o FAT devem comprovar?
The RFQ must describe the complete route and responsibility boundary. FAT should use representative finished LC and SC patch cords from the approved launch range and prove them through the selected cable, connector, fixture, consumable, inspection and optical-test system.
| Acceptance layer | RFQ document | Evidência FAT |
|---|---|---|
| Finished product | Desenho do cabo, componentes do conector, tipo de fibra, comprimento, acabamento e etiqueta | A amostra identificada corresponde à configuração aprovada |
| Limite de responsabilidade | HONGKAI-manufactured, specialist-integrated, buyer-supplied and excluded-item matrix | Every station, utility and test has an owner and open-item status |
| Cabo base quando incluído | Materials, tooling, recipes, package and release plan | Carretéis rastreáveis com buffer apertado e cabo acabado, com registros dimensionais e ópticos acordados |
| Cable preparation | Cut and strip work instructions | Measured length, prepared-end condition and traveler identity |
| Connector assembly | Componente, instruções de adesivo, prensagem e cura | Component and consumable lots, settings and cycle record |
| Polimento e inspeção | Connector-to-fixture matrix, film sequence and inspection criteria | Resultado de face final rastreável para cada amostra FAT |
| Optical test | Wavelength, reference setup, limits, direction and sampling | Resultados registrados de perda por inserção e perda por retorno quando exigidos |
| Work environment | Nível de limpeza, controle de poeira, ar comprimido e condições da bancada de trabalho | Back-end area is clean, low in airborne dust and suitable for the agreed connector process |
| Embalagem e etiquetas | Tampas de proteção contra poeira, campos de etiqueta, método de embalagem e fornecedor responsável | Released sample has the agreed identity, protection and presentation |
| Handover and training | Layout, utilitários, manuais, calibração, peças sobressalentes, consumíveis e divisão de treinamento | HONGKAI trains operators on HONGKAI equipment; the integration partner trains operators on partner equipment |
Lista de verificação:
- ☐ Produtos Launch e famílias de conectores são listados separadamente
- ☐ Cable-making and connector-assembly scopes are separated
- ☐ Cada máquina, fixação, adaptador e consumível tem uma finalidade de produto definida
- ☐ HONGKAI-manufactured, specialist-integrated and buyer-supplied items are explicit
- ☐ Incoming fiber, cable, connector components and consumables have approval rules
- ☐ A inspeção da face final e os testes ópticos estão ambos incluídos quando necessário
- ☐ As amostras FAT utilizam o cabo, conectores, dispositivos e instruções de trabalho acordados
- ☐ The back-end area, compressed air, packing and labels have named owners
- ☐ Training, calibration, maintenance and traceability ownership are assigned
Evidence to request: Keep the approved drawings, equipment configuration, material and component lots, work instructions, operator identity, settings, cure and polish records, inspection images, optical-test setup, raw results, sample labels and a dated open-item list. The separate guia de instalação e comissionamento de linha de fibra óptica fornece uma estrutura de aceitação mais ampla para serviços públicos, documentação, inicialização e entrega.
Note: The complete patch-cord production route is the smallest connected system that can turn approved inputs into a repeatable, traceable finished product. Equipment count alone does not prove that the route is complete.
