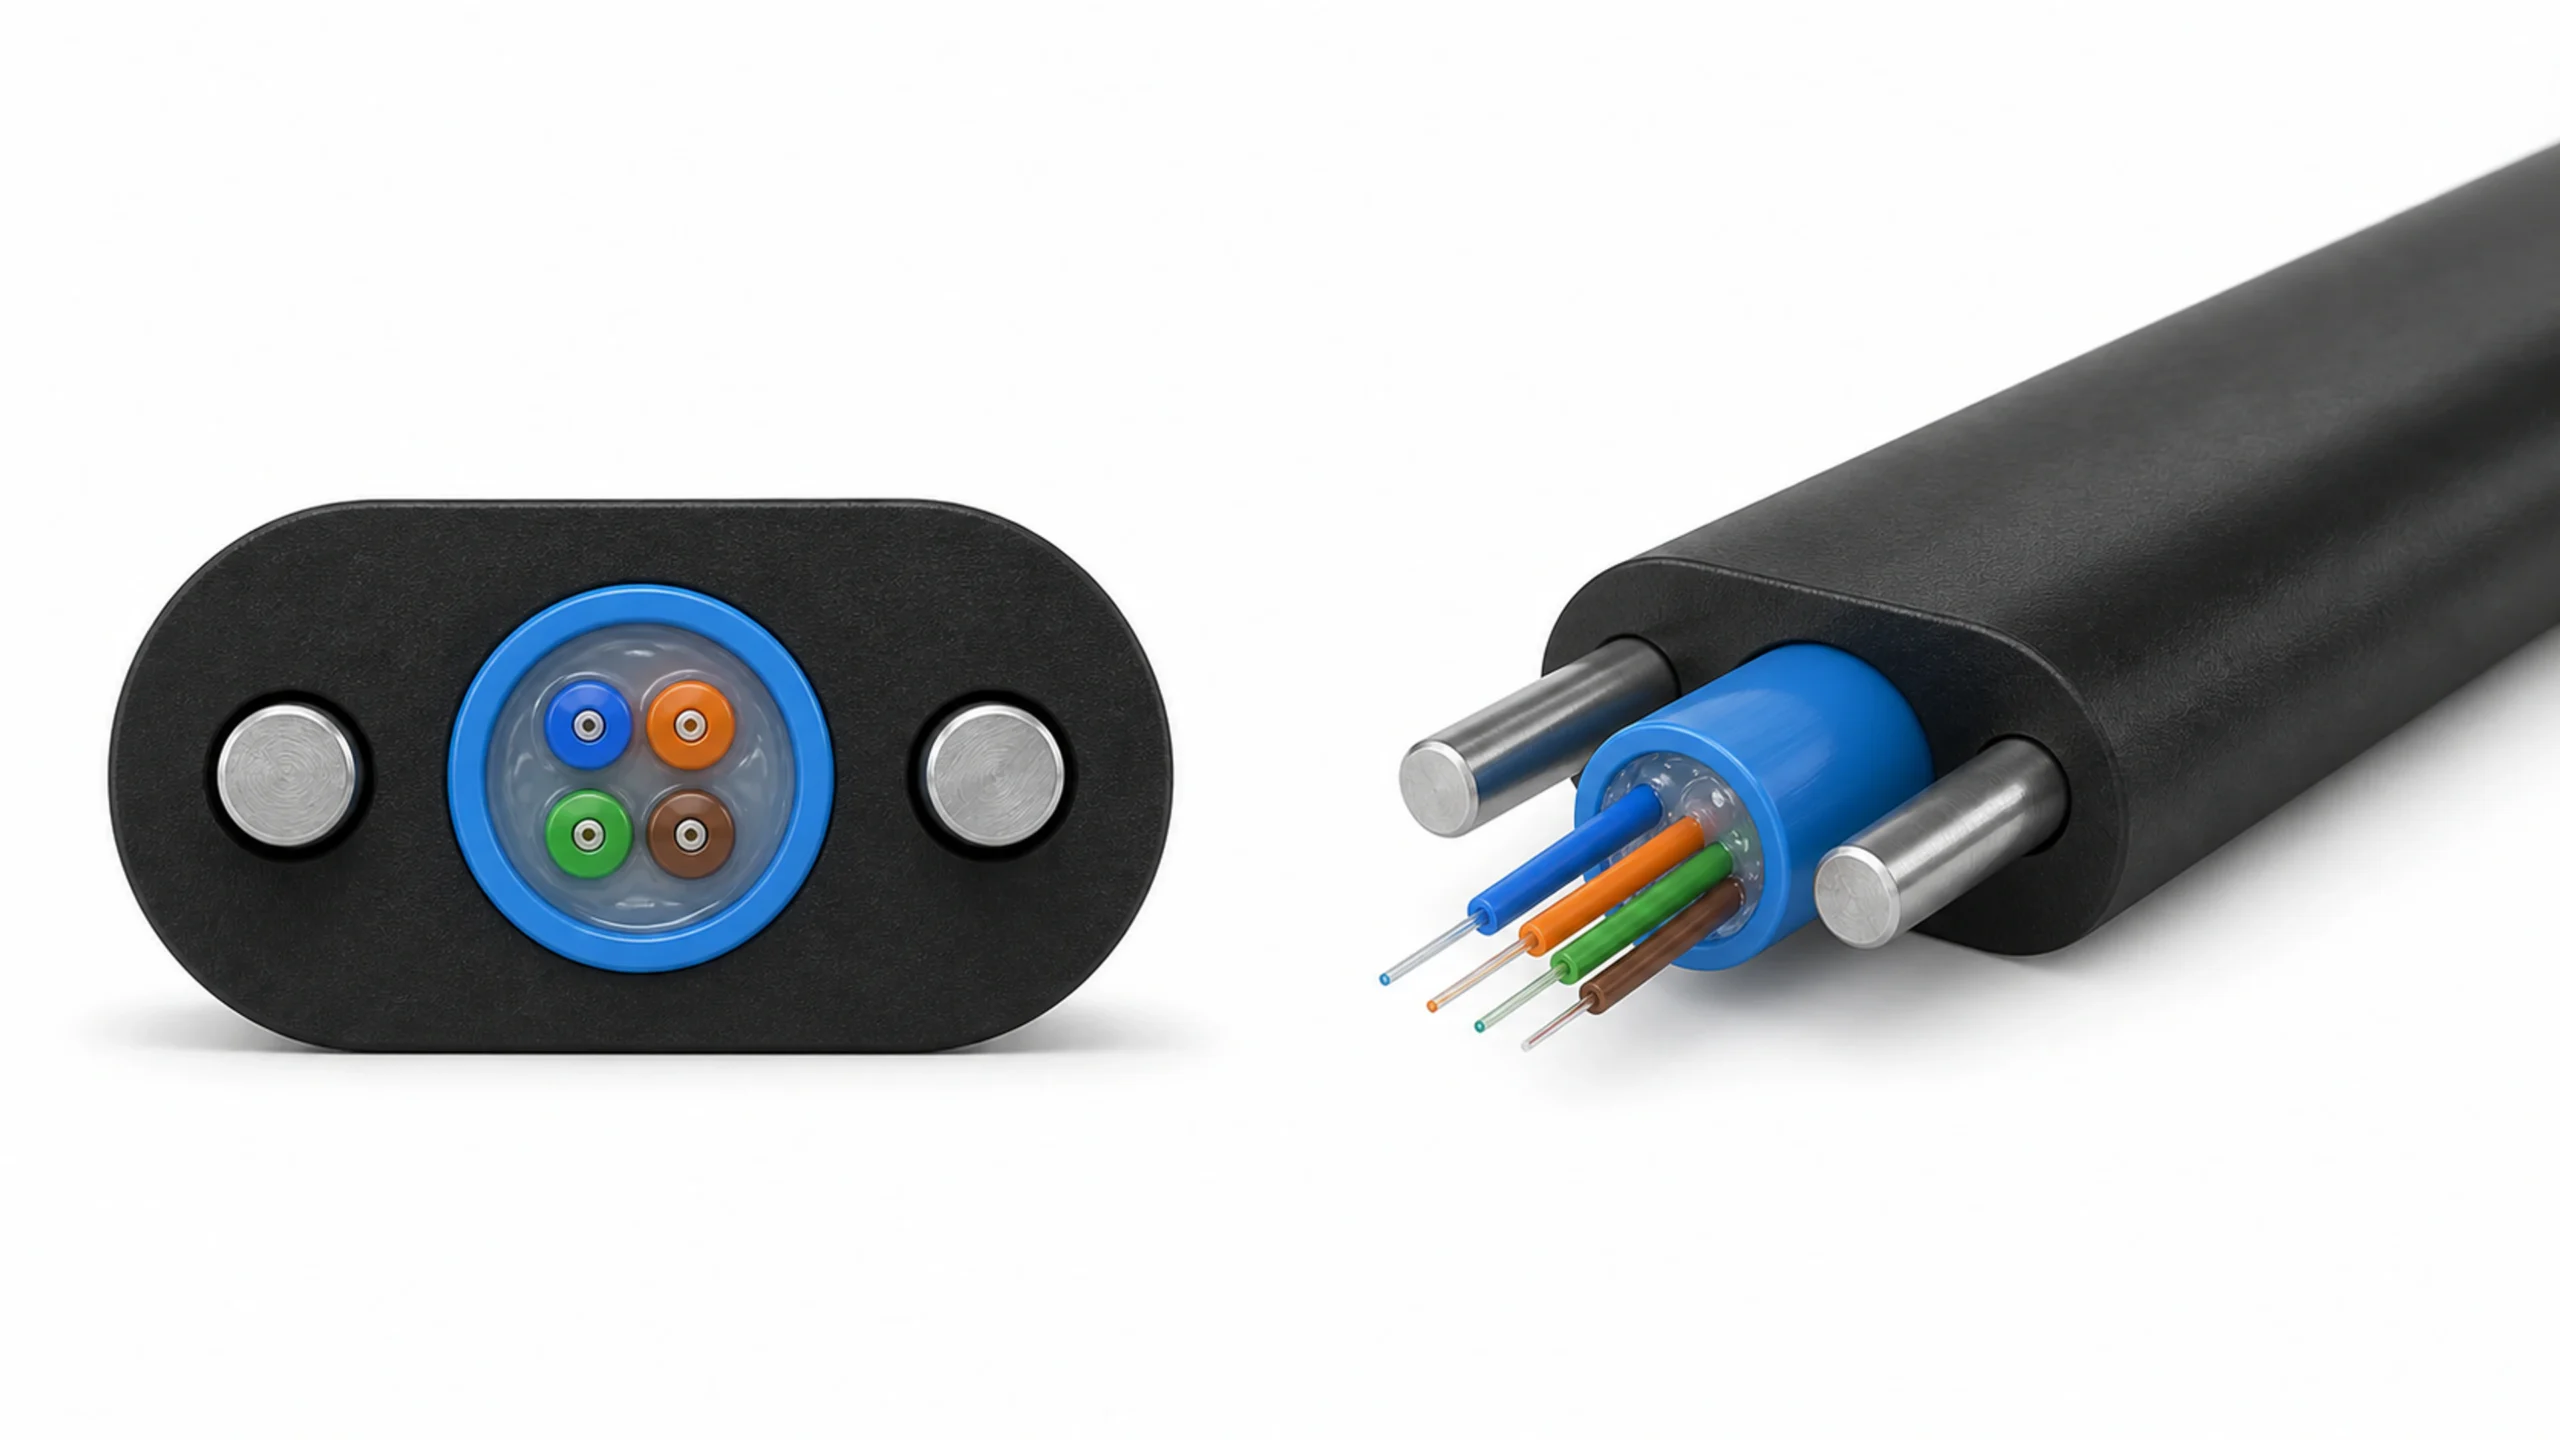



A fiber optic cable factory owner, production manager or technical buyer planning conventional patch cords must define two connected scopes. One scope makes the simplex or duplex base cable; the other cuts that cable and turns each end into an inspected, optically tested connector assembly.
A complete fiber optic patch-cord factory is not one extrusion line. It is either a qualified purchased-cable supply plus a complete connector-assembly workcell, or an integrated route that adds tight-buffer and outer-jacket production before the same back-end workcell.
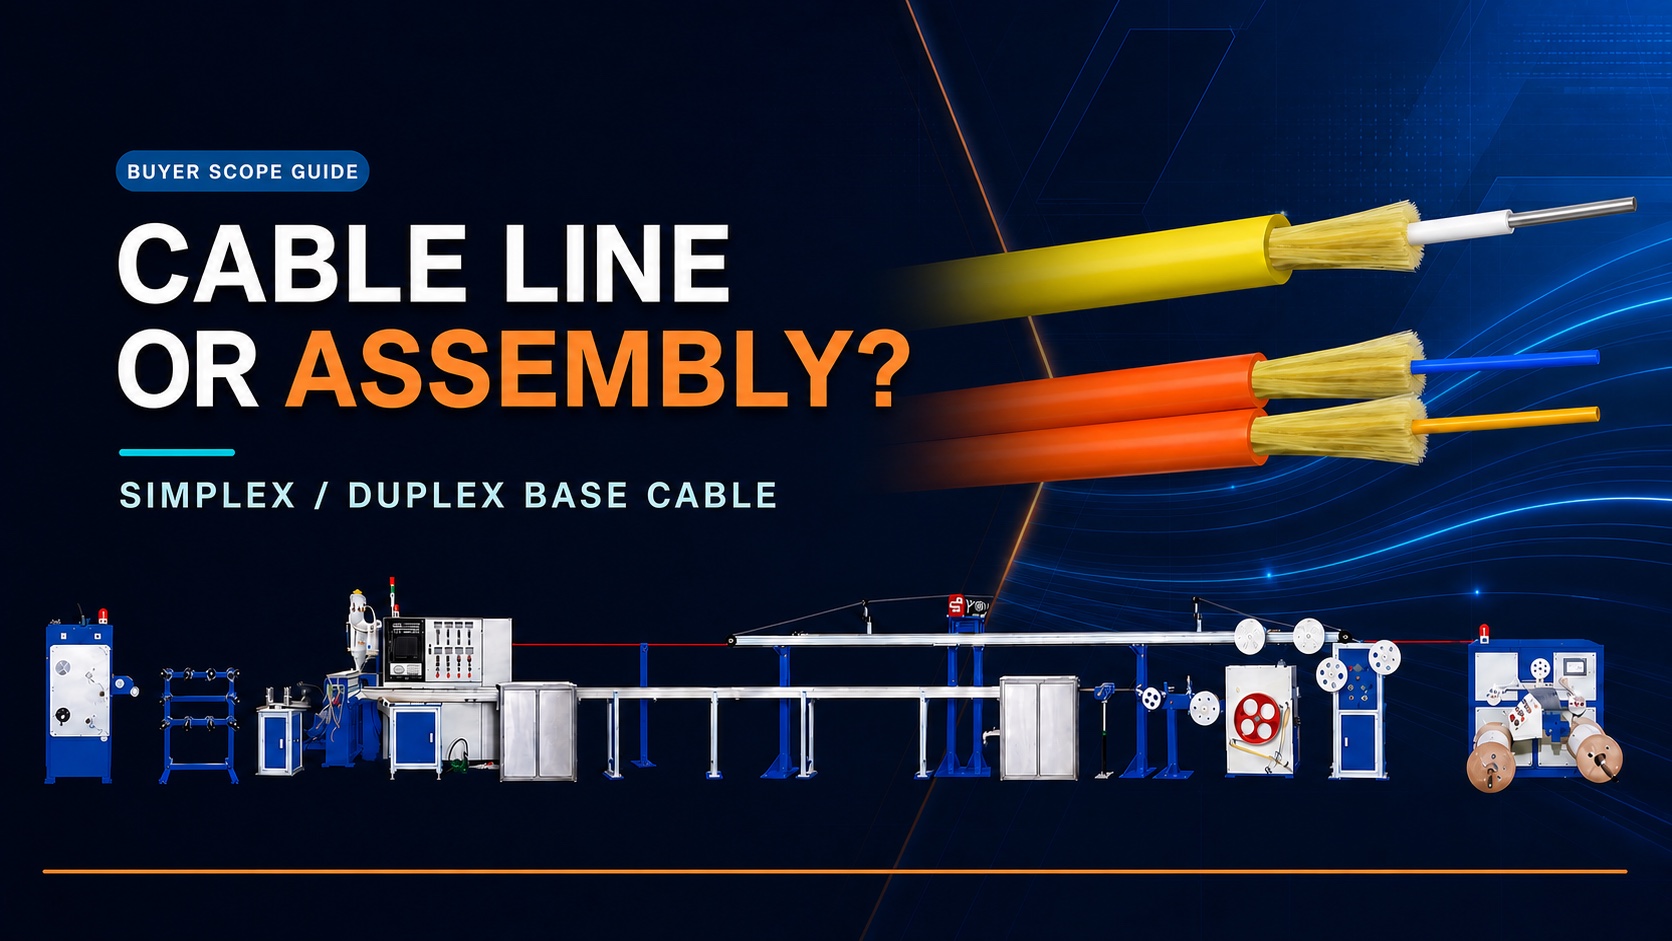
Карта зоны ответственности покупателя: линия производства кабеля изготавливает одножильный или двухжильный базовый кабель; отдельная ячейка сборки разъёмов превращает этот кабель в готовый патч-корд с разъёмами LC или SC.
This guide maps the complete manufacturing boundary for conventional LC and SC patch cords. FC and ST may be added as project-specific fixture variants, but they are not the main production scope in this article. MPO and MTP multi-fiber assemblies are excluded because their cable construction, ferrule preparation, polishing, geometry control, polarity and multi-channel testing require a separate project scope.
Что входит в комплектацию завода по производству патч-кордов?
A complete patch-cord route must end with a saleable, traceable connectorized product—not merely a reel of cable or a visually polished connector. The proposal needs an owner and acceptance record for every stage from incoming fiber or cable through final optical test and packing.
| Manufacturing boundary | Вход | Основной вывод | Доказательства до выпуска |
|---|---|---|---|
| Производство с плотной буферной оболочкой, когда базовый кабель изготавливается собственными силами | Утвержденное оптическое волокно и буферный состав | Квалифицированное волокно с плотным буферным покрытием | Материал, размеры, состояние поверхности и согласованная оптическая проверка |
| Производство арамидной оболочки и наружной оболочки при собственном изготовлении базового кабеля | Утвержденный компаунд для плотного буфера оптического волокна, арамидного волокна и оболочки | Кабель Simplex или Duplex на барабане | Протяжка кабеля, размеры, идентификация барабана, внешний вид и согласованная оптическая проверка |
| Cable preparation | Выпущенная бухта или приобретенный квалифицированный кабель | Обрезанные и подготовленные концы кабеля | Длина, ориентация, размеры полосы и идентификатор тележки |
| Connector assembly | Подготовленный кабель, компоненты разъёмов и утверждённые расходные материалы | Собранные и отвержденные концевые соединители | Партия компонентов, настройки процесса и запись о партии или операторе |
| Полировка и инспекция торцевой поверхности | Стабилизированная сборка разъема | Очистите торцевую поверхность наконечника | Утверждённый процесс полировки и сохранённые или прослеживаемые результаты проверки |
| Оптическое тестирование и отделка | Завершенный патч-корд | Выпущенная реализуемая продукция | Комплект испытательного оборудования, длина волны, результаты, идентификация, маркировка и упаковочный лист |
The HONGKAI patch-cord cable production line supports the base-cable side for applicable constructions. The confirmed project route then adds partner-integrated back-end stations, together with connector-specific fixtures, hand tools and consumables. HONGKAI’s published модель производства и интеграции специалистов explains this source boundary; the final commercial proposal must still distinguish HONGKAI-manufactured equipment, partner-integrated equipment and buyer-supplied items.
Common mistakes: A quotation calls the cable line a complete patch-cord factory but omits connectorization and optical testing. Another quotation lists a polishing machine but omits its connector fixtures, films, inspection adapter, reference cords or process responsibility.
Какие линии HONGKAI формируют базовый кабель?
For the reviewed simplex or duplex construction, the HONGKAI route uses the HK-30 to produce tight-buffered fiber and the HK-50 to apply aramid reinforcement and the outer jacket. If the factory purchases qualified tight-buffered fiber, the cable-making scope can start with the HK-50.
HK-30 стадия натяжной буферизации
The reviewed HK-30 configuration receives optical fiber and applies the specified tight-buffer layer. Its functional modules include controlled payoff, preheating, material drying and feeding, extrusion, warm and cold cooling, online diameter measurement, capstan control and take-up. These functions define the production stage; the customer’s approved construction must define the actual polymer, color, dimensions, reel format and acceptance limits.
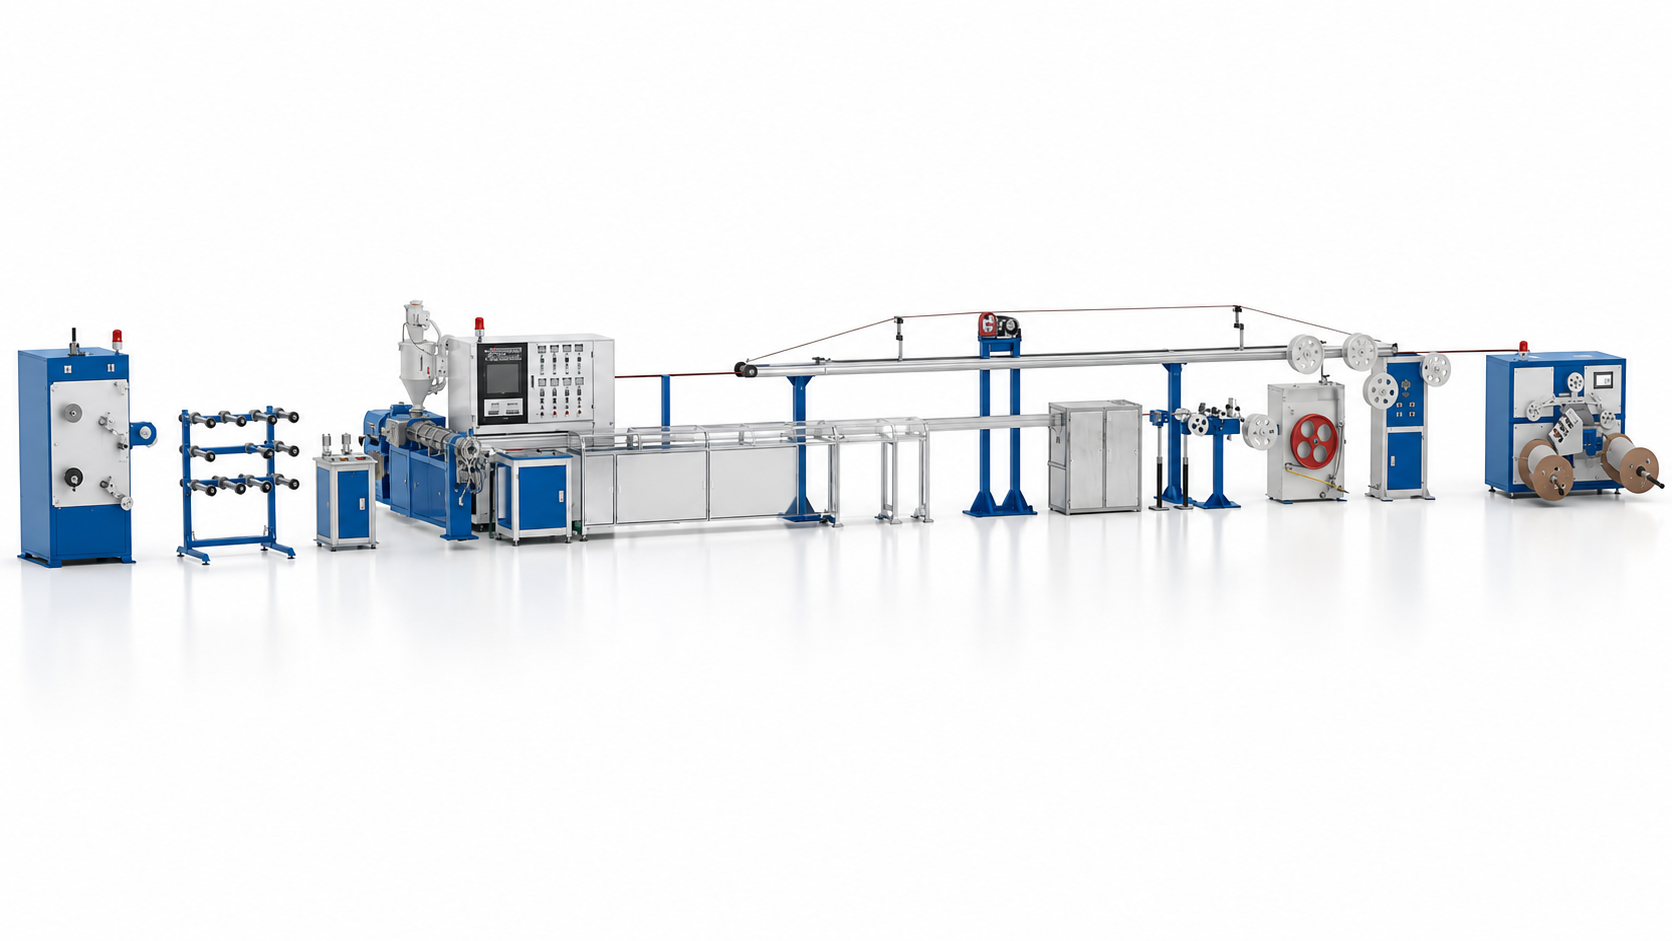
Подтвержденная ссылка HONGKAI HK-30 3D, демонстрирующая полную линию производства уплотнённой оболочки. Окончательная оснастка, материалы и рабочие параметры остаются специфичными для проекта.
HK-50 aramid-and-jacket stage
The reviewed HK-50 configuration receives the approved tight-buffered input, pays off the aramid reinforcement and extrudes the outer jacket. Its functional modules include input payoff, adjustable aramid payoff, positioning, material preparation, extrusion, cooling, online diameter measurement, capstan, accumulation and take-up.

Verified HONGKAI HK-50 3D reference showing the complete line used for an applicable aramid-reinforced simplex or duplex jacket stage. The accepted cable construction controls the final configuration.
The complete in-house route is therefore HK-30 tight buffering followed by HK-50 aramid reinforcement and jacketing. An HK-50-only route is appropriate when the factory has an approved external source for tight-buffered fiber and the incoming package, material, dimensions and optical condition match the signed HK-50 input specification.
The HK-30 and HK-50 documents are older project configurations. They verify the process stages and equipment functions, but their speeds, tensions, power, output, material options and package sizes must not be copied into a new proposal without reconfirmation.
The earlier HONGKAI пошаговое руководство по процессу изготовления патч-корда also shows the HK-30 and HK-50 as separate production stages. Use it as orientation only; the approved cable drawing and current technical agreement control a new project.
How to verify: During FAT, connect the raw-fiber or tight-buffer input to the approved recipe and identify the resulting reel. Retain the actual cable drawing, material lots, tooling, dimensions, surface result, optical check and take-up package used for the trial.
Каков полный процесс производства коммутационного шнура с разъемами LC или SC на стороне производителя?
The supplied conventional LC/SC package covers cable cutting, jacket and buffer stripping, adhesive preparation and dispensing, connector assembly, crimping, curing, fiber scribing, polishing, end-face inspection, optical testing, labeling and packing. The ten powered back-end stations are integrated through HONGKAI’s specialist partner; connector-specific hand tools, fixtures and consumables complete the route.
The sequence below is a controlled planning route for the supplied epoxy-and-polish package. It is not a universal connector recipe. The approved connector-component instructions must set the exact strip dimensions, cleaning method, adhesive, assembly order, crimp tooling, cure cycle, polish sequence and optical limits. A factory should turn those instructions into a traveler or batch record before FAT.
1. Release the incoming cable and production order
Before cutting, verify the cable drawing, connector family, ferrule finish, finished length, quantity, label data and test requirements. Record the incoming reel or cable lot against the work order. If base cable is made in house, the released HK-50 reel is the handoff point; if it is purchased, the supplier’s reel identity and incoming inspection are the handoff evidence.
Как проверить: оператор должен иметь возможность проследить каждый образец FAT до одного утвержденного барабана с кабелем, одной партии компонентов разъема и одной редакции производственной инструкции.
2. Cut the cable to controlled length
The automatic fiber cable cutting machine measures and cuts the released cable for the planned patch-cord length. The RFQ should define the cable-size range, required length range, tolerance, quantity count and whether allowance for stripping and connector assembly is included in the cutting instruction.
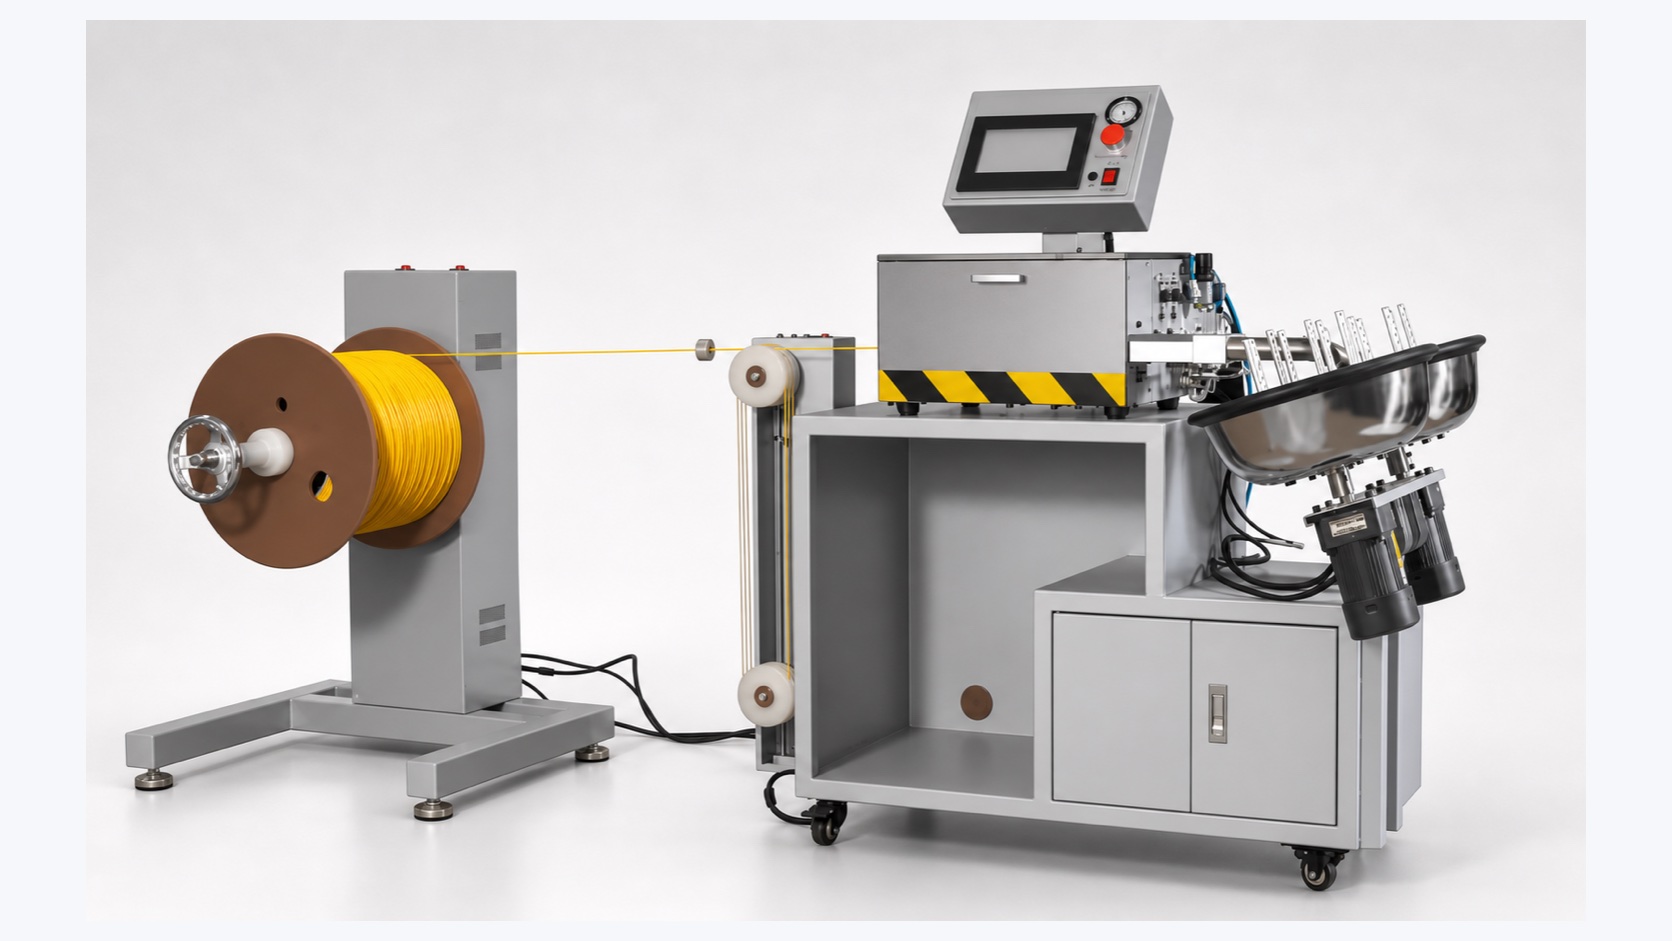
3D technical model based on the verified automatic cable cutting machine in Peter’s supplied conventional patch-cord package. Supplier branding has been removed; this back-end station is integrated through HONGKAI’s specialist partner.
Ловушка: не принимайте только отображаемую длину реза. Во время FAT измерьте определённый образец и сохраните как установленное значение, так и фактические результаты.
3. Strip the outer jacket
The optical cable stripping machine removes the required jacket length so the aramid yarn and buffered fiber can be prepared for the connector. The work instruction must match the actual simplex or duplex cable diameter, jacket material and connector boot or crimp sleeve. Acceptance should cover strip length, a clean cut and no damage to the reinforcement or buffered fiber.
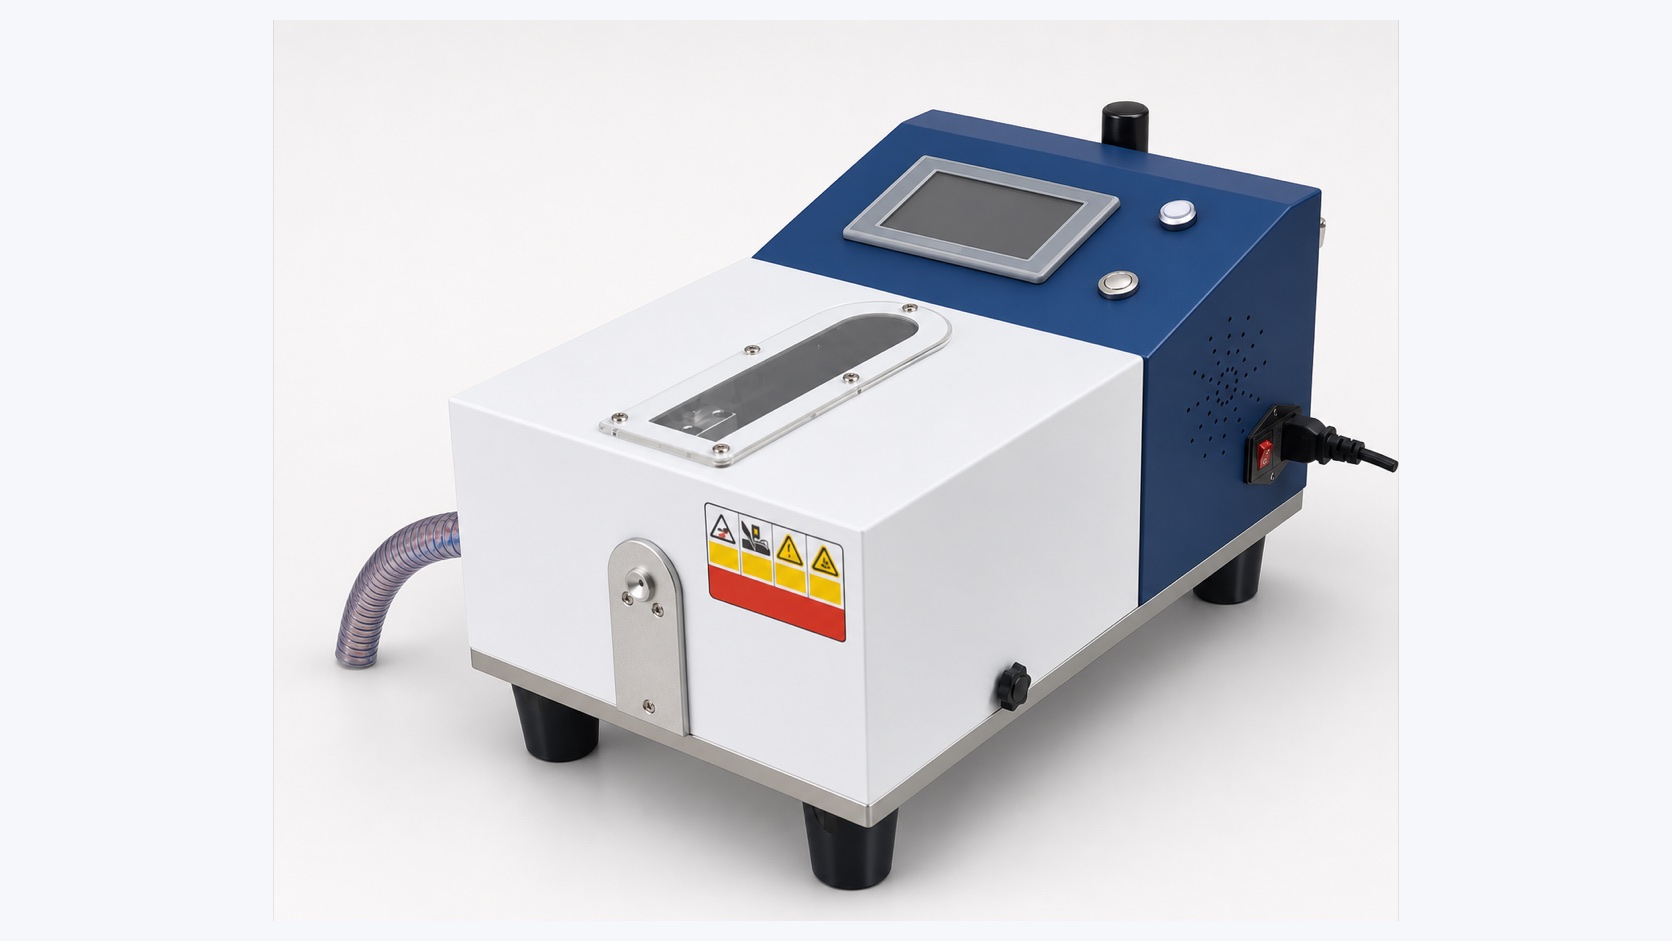
3D technical model based on the verified outer-jacket stripping station. Supplier branding has been removed; final tooling is selected against the approved cable and connector construction.
4. Strip the tight buffer
The buffer stripping machine exposes the glass fiber to the dimension required by the connector assembly process. The operator must control the strip length and inspect the exposed fiber for coating residue, scratches or breakage. The machine does not replace cleaning and handling discipline.
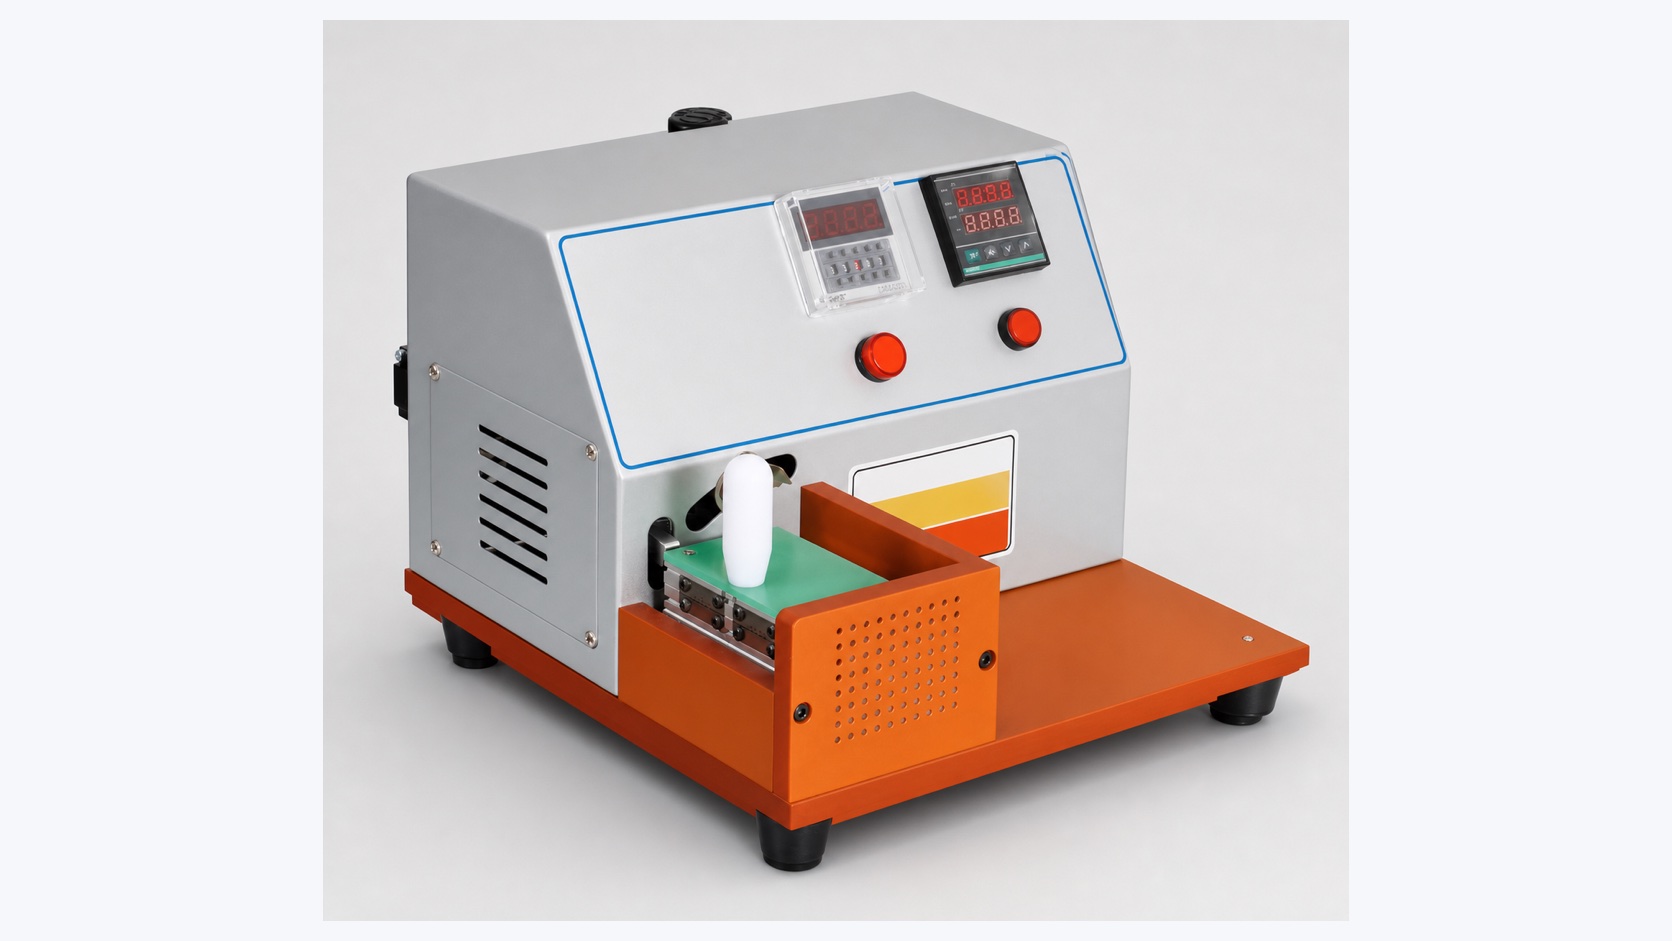
3D technical model based on the verified tight-buffer stripping station in the supplied LC/SC package. Supplier branding has been removed.
Что спрашивать: запросите допустимый диапазон кабеля и буфера, список сменных лезвий или оснастки, метод проверки длины зачистки и критерии отбраковки поврежденного волокна.
5. Prepare adhesive with the Model 800 centrifuge
For the reviewed epoxy-and-polish route, the approved adhesive is prepared according to its supplier instruction. The Model 800 epoxy centrifuge supports controlled preparation and removal of entrained air before dispensing. Adhesive identity, mix ratio when applicable, preparation time, usable life, storage condition and disposal rule belong in the batch record.
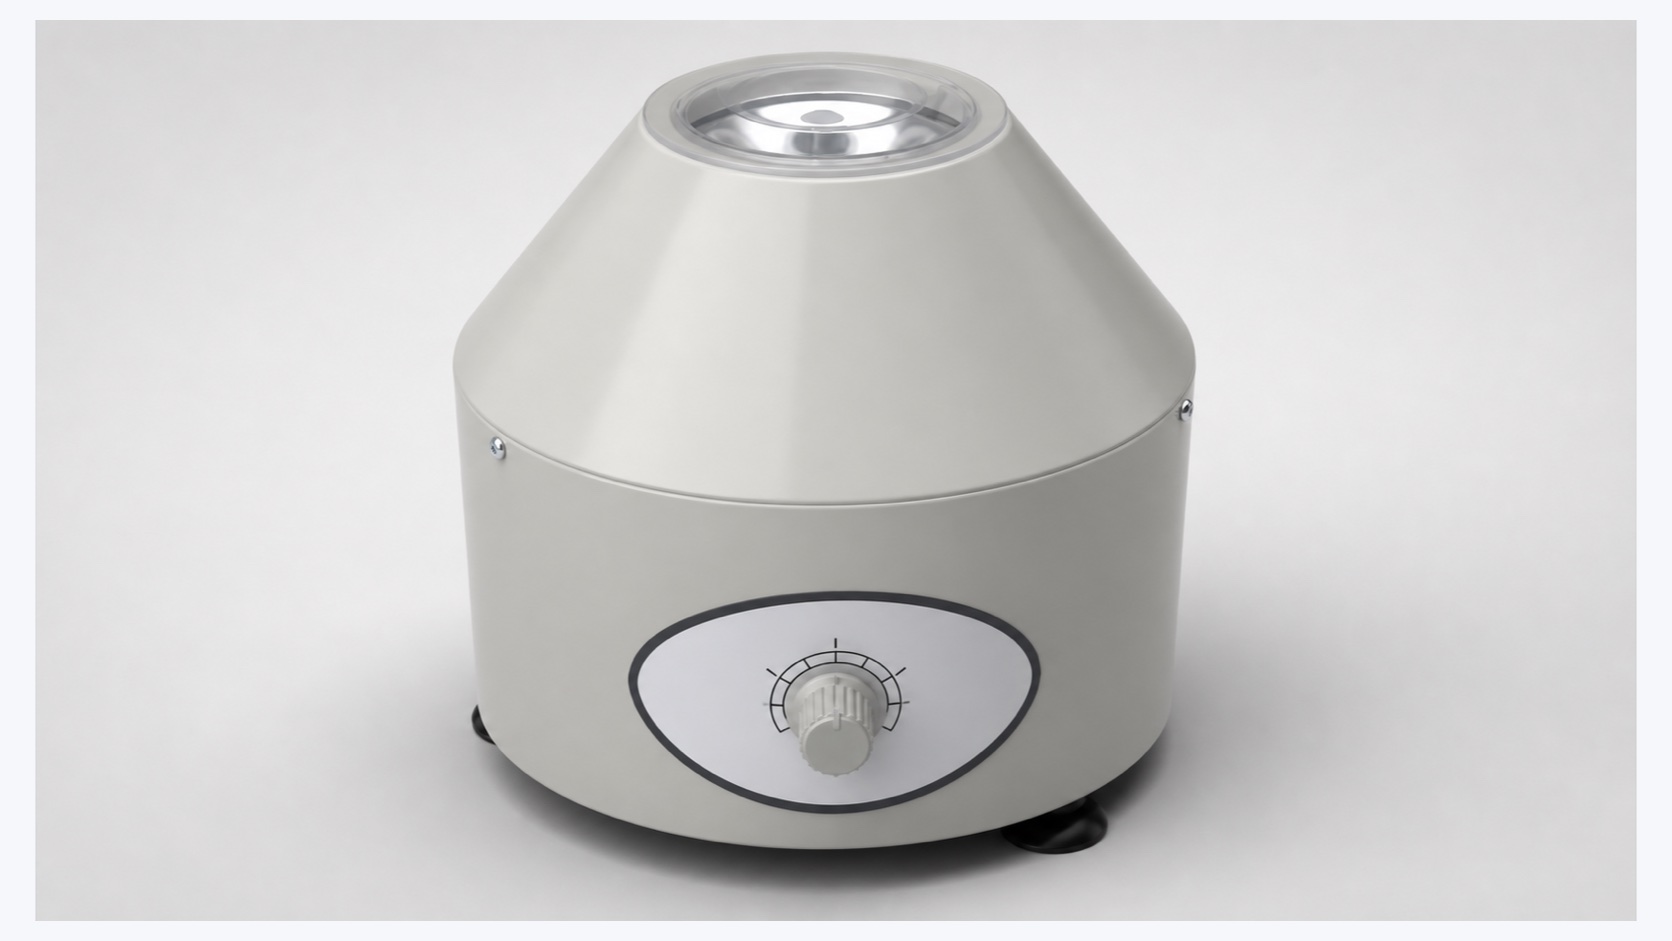
3D technical model based on the verified epoxy centrifuge in the supplied package. Supplier markings have been removed; the approved connector and adhesive suppliers—not the image—define the preparation recipe.
Ловушка: список оборудования, в котором указано только “эпоксидная смола”, оставляет покупателя без совместимой клеевой системы, контроля партии или правила определения срока годности.
6. Dispense the adhesive
The epoxy dispenser delivers the prepared adhesive to the connector assembly process. The dispensing needle or adapter, dose, cleaning interval and confirmation method must suit the selected LC or SC connector components. Record the adhesive batch and preparation time with the work order.
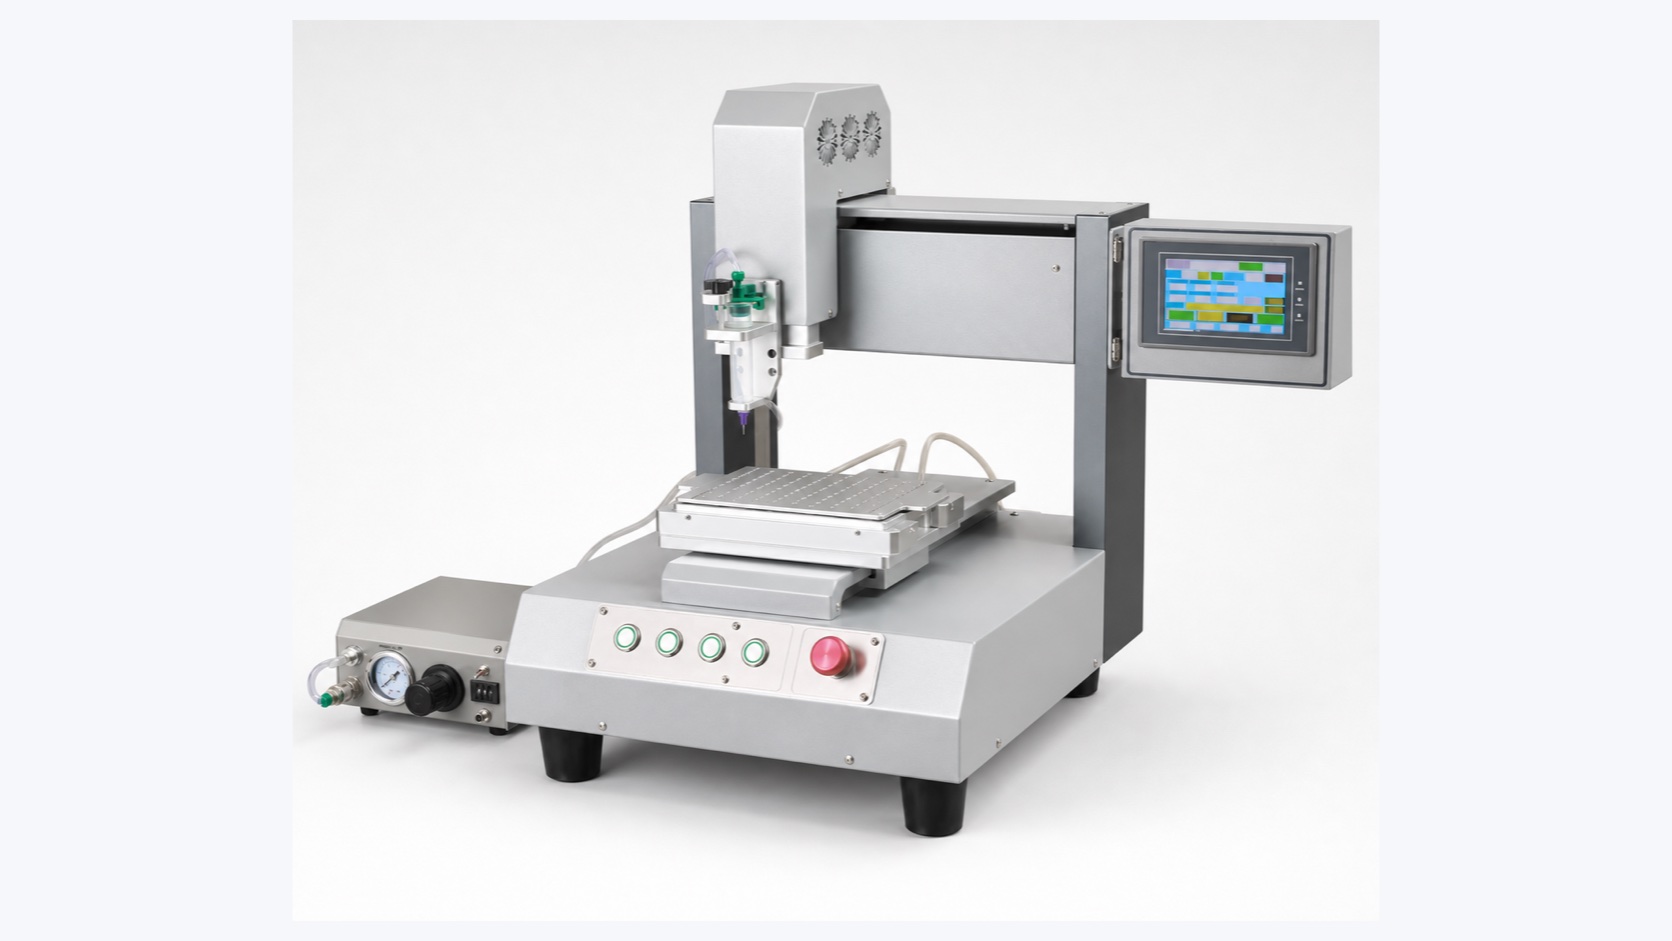
3D technical model based on the verified adhesive dispensing station in the supplied conventional connector route. Supplier branding has been removed.
7. Insert the fiber, assemble components and crimp
The operator threads the prepared fiber into the ferrule, seats the cable and assembles the boot, crimp sleeve and other specified parts in the connector supplier’s approved order. The pneumatic crimping machine applies the connector-specific crimp through the correct die or fixture. The factory must provide stable compressed air at the agreed pressure and quality.

3D technical model based on the verified pneumatic crimping machine. Supplier branding has been removed; the connector construction controls the die, crimp position and acceptance check.
How to verify: Inspect component seating, aramid capture, boot position and crimp condition on representative LC and SC assemblies. Record the die or fixture identity and compressed-air condition used for FAT.
8. Cure the connector assembly
The curing oven stabilizes the adhesive under the approved time-and-temperature instruction. The work instruction must define loading orientation, fixture or holder, setpoint, actual cycle evidence, batch size and handling after cure. Do not transfer a cure recipe from another adhesive or connector system without approval.

3D техническая модель на основе проверенного разъёма с блоком отверждения в поставляемом комплекте LC/SC. Бренд поставщика удалён.
Требуемые доказательства: В сопроводительных документах на приёмосдаточные испытания (FAT) каждая проба должна быть привязана к партии клея, идентификатору печи, записи цикла и ответственному оператору.
9. Надрезать лишнее волокно и подготовить ферруль к полировке
After the approved cure and cooling sequence, use the specified fiber cutting pen or scribing tool to remove the protruding fiber without chipping the ferrule or damaging the fiber. Clean the connector and polishing fixture before loading. This is a hand-tool step in the supplied package, not a reason to invent another machine.
Типичные ошибки: чрезмерное усилие при нанесении надрезов, попадание загрязнений в полировочное приспособление и отсутствие правила замены изношенного ручного инструмента.
10. Отполируйте феррулы LC и SC
The fiber connector polishing machine performs the mechanical polishing stage. A complete station also needs the correct LC or SC holder, the approved UPC or APC process where applicable, polishing pads and films, cleaning materials and a controlled film-change rule. Peter’s supplied package lists connector-specific fixtures; they must be scheduled by actual launch product rather than assumed from the machine name.
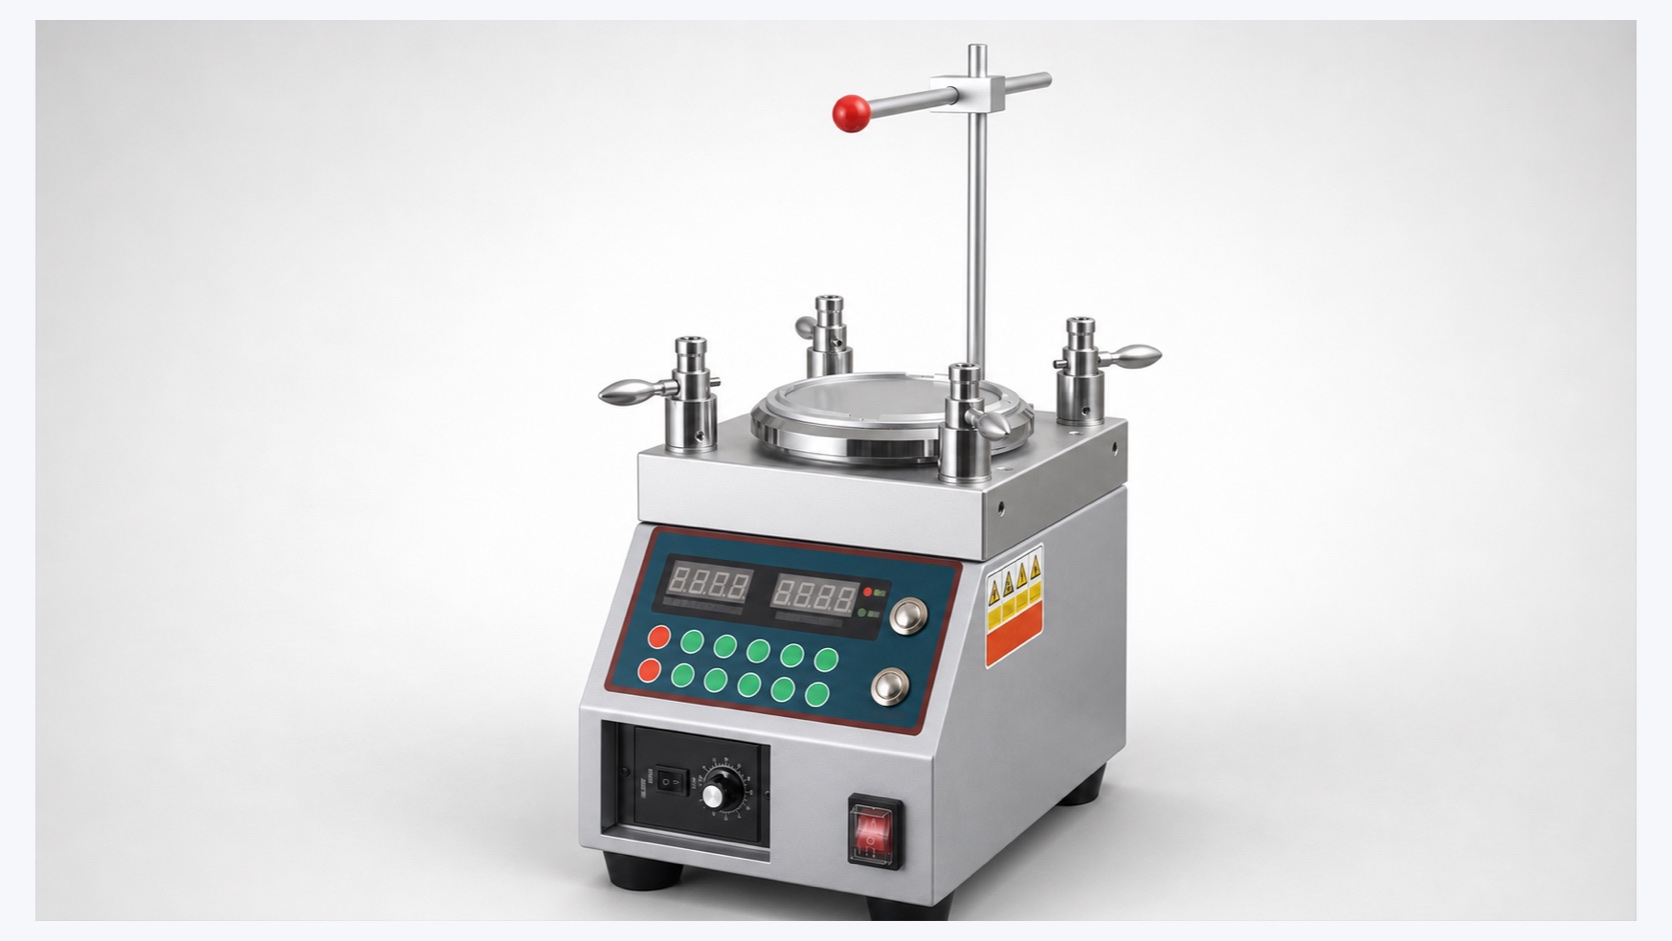
3D technical model based on the verified polishing machine in the supplied package. Supplier branding has been removed; LC and SC require the correct connector-specific holder and approved consumable sequence.
What to ask: Require a connector-to-fixture matrix, film sequence, cleaning step, process ownership and replacement plan. A polishing machine without the right holder and consumables is not a working LC/SC station.
11. Очистите и осмотрите торцевую поверхность
After polishing, clean the connector with the approved materials and inspect it using the fiber connector inspection microscope with the correct adapter. The acceptance record should distinguish contamination that can be cleaned from scratches, chips or other defects that require rework or rejection.
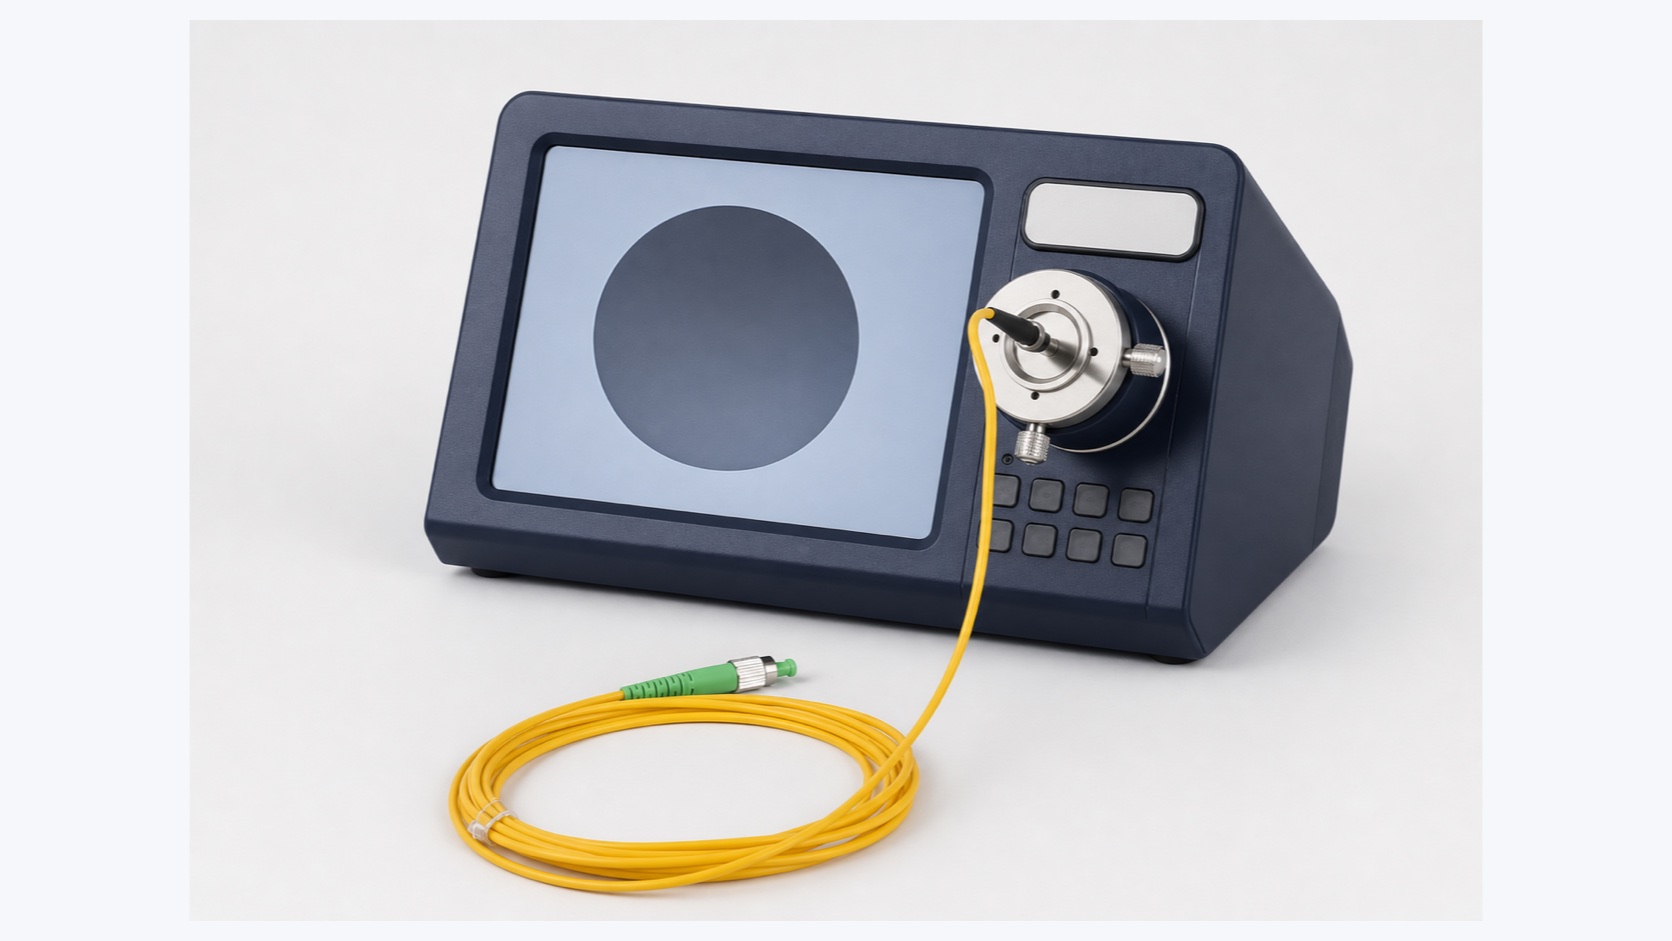
3D technical model based on the verified ferrule inspection microscope in the supplied LC/SC workcell. Supplier branding has been removed.
IEC 61300-3-35:2022 covers visual inspection and classification of contamination, scratches and defects on fibre-optic connector interfaces. The product specification still needs to identify the applicable connector interface, inspection method and acceptance criteria. Visual inspection does not replace finished-product optical testing.
12. Measure insertion loss and return loss with the 7420B
The 7420B insertion-loss and return-loss tester is the final powered test station in the supplied package. Before FAT, define fiber type, wavelength, reference method, connector adapters, reference cords, test direction, acceptance limits, calibration responsibility and how each result is tied to the finished patch cord.
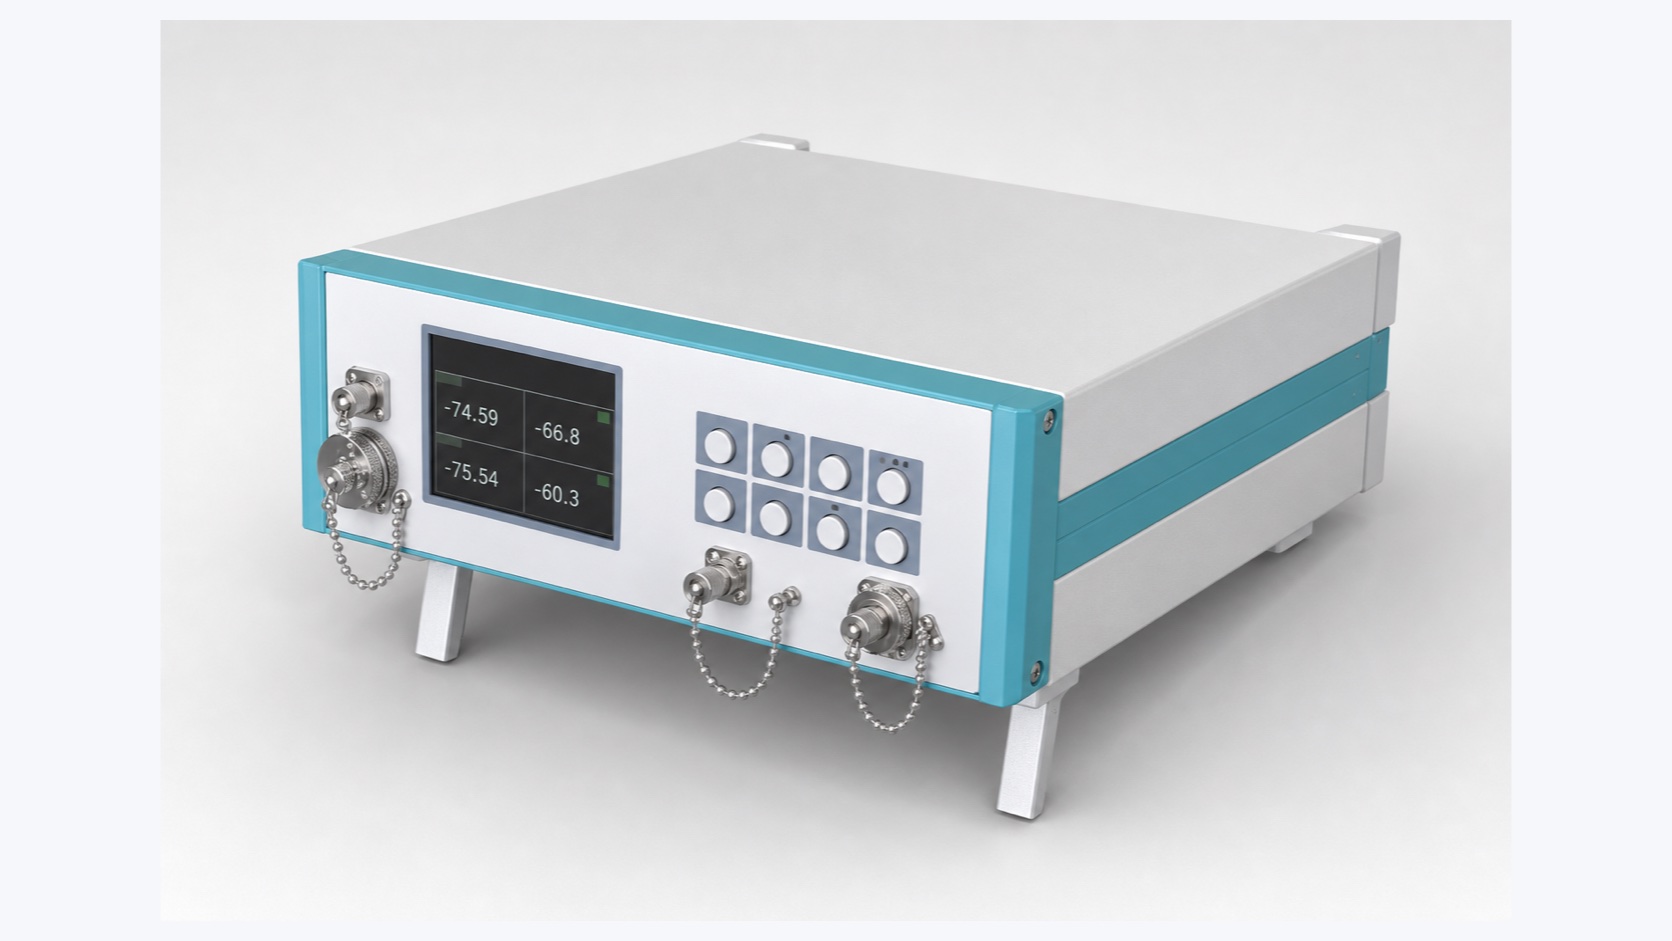
3D technical model based on the verified optical tester in the supplied package. Supplier branding has been removed; the station supports traceable insertion-loss and return-loss testing of the finished conventional patch cord.
IEC 61300-3-4:2023 рассматривает методы измерения затухания, в то время как IEC 61300-3-6:2008 addresses return-loss measurement procedures. These references do not supply the product’s pass/fail values; those values must come from the approved product specification and customer agreement.
13. Perform final visual checks, label and pack
Use the visual fault locator when it belongs to the agreed work instruction, complete the final visual and dimensional checks, fit clean dust caps, apply the traceable label and pack the patch cord so the connector end faces and cable bend condition are protected. The released sample should carry the product code, length, connector configuration, fiber or cable identity, batch or serial reference and test status required by the buyer’s system.
The connector-processing area should be clean and have little airborne dust; a cleanroom is preferable when the product and quality requirements justify it. The layout must separate dirty preparation work from cleaned ferrules and finished connectors. The RFQ should assign compressed air, benches, lighting, cleaning materials, waste handling, labels and packaging instead of assuming they are included with the machines.
Pitfalls: The workcell depends on operator memory for strip length or polishing steps, end-face images are not tied to product identity, optical results have no documented reference method, or tested connectors are exposed to dust again before capping and packing.
Сводка по вспомогательному оборудованию
| Process stage | Reference equipment | Требуемое смежное управление |
|---|---|---|
| Length cutting | Автоматический станок для резки кабеля | Допуск по длине, допуск и измерение образца |
| Jacket stripping | Стриппер для оптического кабеля | Оснастка и критерии повреждений, специфичные для кабеля |
| Buffer stripping | Стриппер для плотного буфера | Осмотр и очистка состояния волокна |
| Adhesive preparation | Model 800 | Журнал идентификации, смешивания и срока годности клея |
| Adhesive dispensing | Epoxy dispenser | Дозирование, адаптер и контроль очистки |
| Connector crimping | Пневматический обжимной станок | Матрица, специфичная для разъёма, и сжатый воздух |
| Curing | Сушильная печь для разъемов | Утвержденная прослеживаемость циклов и партий |
| Ferrule polishing | Машина для полировки волоконно-оптических разъёмов | Фиксатор LC/SC, пленки и последовательность очистки |
| Инспекция торцевой поверхности | Микроскоп для контроля волоконных соединителей | Адаптер, критерии и прослеживаемый результат |
| Optical testing | 7420B | Длина волны, эталонная установка, пределы и калибровка |
Which Fixtures, Tools and Consumables Belong in the RFQ?
Fixtures and consumables are part of the manufacturing system because they determine which connectors can be processed and whether the result is repeatable. A machine without the correct holder, film, adapter or cleaning control is not a complete station.
Peter’s supplied package names LC and SC polishing fixtures, including UPC and APC variants where applicable. FC and ST fixtures are also available in the reference package, but they should be added only when those connector families belong to the approved product list. The package also includes fiber and cable strippers, crimping pliers, aramid scissors, a fiber cutting pen, an electronic balance, adhesive, polishing pads and films, a visual fault locator and cleaning paper.
| Scope group | Элементы для планирования | Решение покупателя |
|---|---|---|
| Connector fixtures | Держатели для полировки, адаптеры для контроля, испытательные адаптеры и любая оснастка для обжима или сборки | Перечислите все семейства разъемов, типы полировки феррул и поставщиков компонентов |
| Ручные инструменты для подготовки | Съемник оптического волокна, съемник оболочки, ножницы для арамидных нитей, режущий инструмент и обжимные клещи | Определите количество замены, распределение операторов и метод контроля |
| Adhesive controls | Клей, инструменты для взвешивания или смешивания, центрифуга, дозатор и чистящие средства | Заморозьте совместимую клеевую систему и элементы контроля хранения, подготовки и срока годности |
| Polishing consumables | Прокладки, пленки и чистящие материалы | Утвердить последовательность, марку, поставщика, правило изменения и контроль партии |
| Test accessories | Эталонные шнуры, адаптеры, оправки или элементы режимной обработки при необходимости, а также визуальный индикатор неисправностей | Определите метод испытаний, интерфейсы разъемов и ответственность за калибровку |
| Finishing materials | Пылезащитные колпачки, этикетки и упаковочные материалы | Определите чистоту, идентификацию, внешний вид и защиту при транспортировке |
What to ask: Require a connector-to-fixture matrix and a consumable list for the launch products. The supplier should state which items are included, which wear out, which require regular replacement and which must be sourced from the connector or consumable manufacturer.
Должен ли новый завод покупать базовый кабель или производить его собственными силами?
Start with the narrowest complete route that can release the intended saleable patch cord. Buying qualified cable concentrates investment and training on connector assembly; adding HK-30 and HK-50 brings cable construction and supply control in house but also adds extrusion, material, reel and intermediate-quality responsibilities. Более широкий маршрутная карта производства оптоволоконного кабеля помогает покупателям размещать этот узкий маршрут для внутреннего кабеля рядом с другими семействами линий оптических кабелей, не рассматривая один список оборудования как универсальный.
| Decision factor | Покупайте квалифицированный базовый кабель | Добавить собственное производство базовых кабелей |
|---|---|---|
| Начальный объем процесса | Квалификация входящего кабеля и сборка разъема | Обработка плотного буфера, арамидного волокна и оболочки, а также сборка разъёмов |
| Контроль основного поставщика | Протяжка кабеля, записи на барабанах и уведомление об изменении | Волокно, составы, оснастка, рецептуры, прослеживаемость кабеля в процессе производства и на барабане |
| Навыки для развития | Подготовка, обжимка, полировка, инспекция и оптическое тестирование | Все навыки сборки, а также экструзия, охлаждение, контроль натяжения и намотки |
| Expansion constraint | Утвержденный портфель поставщиков и условия сроков поставки | Проверены окно оборудования, оснастка, материал и план переналадки |
| Handoff risk | Утверждение входящей катушки в маршрутной карте сборки | HK-30 output to HK-50, then finished reel to connector assembly |
Decision criterion: Compare the approved product mix, cable-source reliability, process knowledge, staffing, quality system and traceability burden. Do not justify the integrated route only with an unsupported production-volume or payback threshold.
Red flags: A proposal adds cable extrusion without an intermediate-reel release plan, or assumes that owning the cable line automatically reduces finished-patch-cord defects. Control improves only when materials, work instructions, operators and evidence are qualified together.
Почему MPO исключён из этого маршрута оборудования?
MPO is excluded because both its incoming multi-fiber cable and its connector-assembly workcell can differ from conventional single-fiber patch cords. A polishing fixture alone does not convert the ordinary patch-cord route into an MPO route.
The supplied specialist catalog separates the ordinary patch-cord machines from a dedicated MPO/MTP group. That group includes multi-fiber-specific preparation, polishing fixtures, curing, end-face or geometry inspection, polarity or channel control and multi-channel optical testing. Peter’s supplied experience also identifies more stable automatic polishing pressure as an important MPO consideration because one connector presents multiple fibers to the polishing process.
This article therefore stops at conventional single-fiber connector families. A separate MPO article must begin with the exact cable construction, fiber count, ferrule and connector system, polarity, end-face geometry requirement and channel-test method before selecting equipment.
Note: The supplied conversation mentions a project range of multiple fibers per MPO connector. That range remains a bounded project observation and will not be published as a universal MPO specification without Peter’s confirmation.
Что должны подтвердить RFQ и FAT?
The RFQ must describe the complete route and responsibility boundary. FAT should use representative finished LC and SC patch cords from the approved launch range and prove them through the selected cable, connector, fixture, consumable, inspection and optical-test system.
| Acceptance layer | RFQ document | Доказательства FAT |
|---|---|---|
| Готовая продукция | Протяжка кабеля, компоненты разъема, тип волокна, длина, отделка и маркировка | Идентифицированный образец соответствует утвержденной конфигурации |
| Граница ответственности | HONGKAI-manufactured, specialist-integrated, buyer-supplied and excluded-item matrix | За каждой станцией, вспомогательной системой и испытанием закреплен владелец и статус незавершенных вопросов |
| Базовый кабель при наличии | Материалы, оснастка, рецептуры, упаковка и план выпуска | Проследимые бухты с плотным буфером и готовым кабелем с согласованными размерными и оптическими характеристиками |
| Cable preparation | Инструкции по резке и зачистке | Измеренная длина, состояние с подготовленными концами и идентификатор перемещения |
| Connector assembly | Компонент, инструкции по нанесению клея, обжиму и отверждению | Партии компонентов и расходных материалов, настройки и запись цикла |
| Полировка и инспекция | Матрица соединителя с оснасткой, последовательность пленок и критерии проверки | Трассируемый результат торцевой поверхности для каждого образца FAT |
| Optical test | Длина волны, эталонная установка, пределы, направление и выборка | Зарегистрированные результаты измерения вносимых потерь и потерь на отражение при необходимости |
| Work environment | Уровень чистоты, контроль пыли, сжатый воздух и условия на верстаке | Back-end area is clean, low in airborne dust and suitable for the agreed connector process |
| Packing and labels | Пылезащитные колпачки, поля для маркировки, метод упаковки и ответственный поставщик | Выпущенный образец имеет согласованные идентификацию, защиту и оформление |
| Handover and training | Layout, utilities, manuals, calibration, spares, consumables and training split | HONGKAI trains operators on HONGKAI equipment; the integration partner trains operators on partner equipment |
Чек-лист:
- ☐ Продукты Launch и семейства разъёмов перечислены отдельно
- ☐ Области производства кабелей и сборки разъёмов разделены
- ☐ Every machine, fixture, adapter and consumable has a named product purpose
- ☐ HONGKAI-manufactured, specialist-integrated and buyer-supplied items are explicit
- ☐ Incoming fiber, cable, connector components and consumables have approval rules
- ☐ Осмотр торцевой поверхности и оптическое тестирование включены в необходимых случаях
- ☐ FAT samples use the agreed cable, connectors, fixtures and work instructions
- ☐ The back-end area, compressed air, packing and labels have named owners
- ☐ Training, calibration, maintenance and traceability ownership are assigned
Evidence to request: Keep the approved drawings, equipment configuration, material and component lots, work instructions, operator identity, settings, cure and polish records, inspection images, optical-test setup, raw results, sample labels and a dated open-item list. The separate руководство по установке и вводу в эксплуатацию линии оптоволокна обеспечивает более широкую основу для принятия коммунальных услуг, документации, запуска и передачи.
Note: The complete patch-cord production route is the smallest connected system that can turn approved inputs into a repeatable, traceable finished product. Equipment count alone does not prove that the route is complete.