


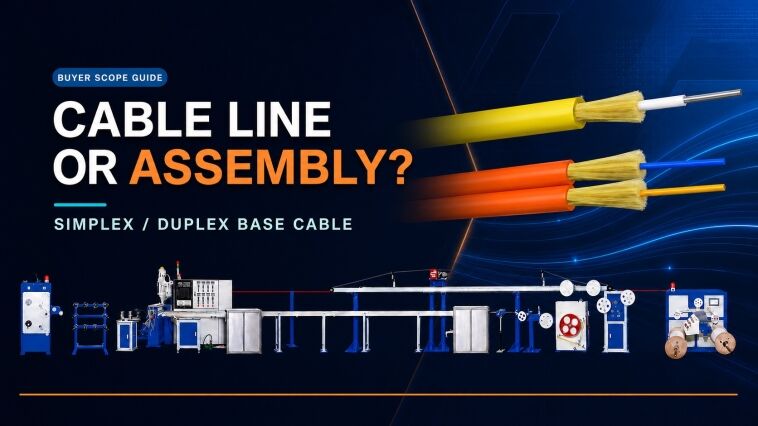
A fiber optic cable factory owner, production manager or technical buyer planning conventional patch cords must define two connected scopes. One scope makes the simplex or duplex base cable; the other cuts that cable and turns each end into an inspected, optically tested connector assembly.
A complete fiber optic patch-cord factory is not one extrusion line. It is either a qualified purchased-cable supply plus a complete connector-assembly workcell, or an integrated route that adds tight-buffer and outer-jacket production before the same back-end workcell.

خريطة نطاق المشتري: خط إنتاج الكابلات يصنع كابلًا أساسيًا مفردًا أو مزدوجًا؛ وخلية عمل تجميع الموصلات المنفصلة تحول هذا الكابل إلى سلك توصيل جاهز بنوعي الموصل LC أو SC.
This guide maps the complete manufacturing boundary for conventional LC and SC patch cords. FC and ST may be added as project-specific fixture variants, but they are not the main production scope in this article. MPO and MTP multi-fiber assemblies are excluded because their cable construction, ferrule preparation, polishing, geometry control, polarity and multi-channel testing require a separate project scope.
ما الذي يشمله مصنع كامل للكابلات التوصيلية؟
A complete patch-cord route must end with a saleable, traceable connectorized product—not merely a reel of cable or a visually polished connector. The proposal needs an owner and acceptance record for every stage from incoming fiber or cable through final optical test and packing.
| Manufacturing boundary | المدخل | الإخراج الرئيسي | الدليل قبل الإصدار |
|---|---|---|---|
| إنتاج الغلاف الضيق عندما يُصنع الكابل الأساسي داخليًا | مركب الألياف الضوئية والغلاف المعتمد | ألياف مؤهلة ذات غلاف ضيق | هوية المادة، الأبعاد، حالة السطح والفحص البصري المتفق عليه |
| إنتاج الأراميد والغلاف الخارجي عندما يُصنع الكابل الأساسي داخليًا | مركب الألياف ذات الغلاف الضيق المعتمد، والأراميد والغلاف | كابل سيمبلكس أو دوبلكس على بكرة | رسم الكابل، الأبعاد، هوية البكرة، المظهر والفحص البصري المتفق عليه |
| Cable preparation | بكرة مفرغة أو كابل مؤهل تم شراؤه | أطراف الكابلات المقطوعة والمحضّرة | الطول، الاتجاه، أبعاد الشريط، وهوية المسافر |
| Connector assembly | الكابلات المحضّرة، مكونات الموصلات والمستهلكات المعتمدة | أطراف الموصلات المجمعة والمعالَجة حرارياً | دفعة المكونات، وإعدادات العملية، وسجل الدُفعة أو المشغّل |
| فحص الوجه النهائي والتلميع | مجموعة توصيل مستقرة | نظّف الطرف الأمامي للحلقة | عملية التلميع المعتمدة ونتيجة الفحص المخزنة أو القابلة للتتبع |
| الاختبار البصري والتشطيب | سلك توصيل جاهز | المنتج القابل للبيع الذي تم إصداره | إعداد الاختبار، الطول الموجي، النتائج، الهوية، الملصق وسجل التغليف |
ال خط إنتاج كابلات سلك التوصيل HONGKAI supports the base-cable side for applicable constructions. The confirmed project route then adds partner-integrated back-end stations, together with connector-specific fixtures, hand tools and consumables. HONGKAI’s published نموذج التصنيع والتكامل المتخصص explains this source boundary; the final commercial proposal must still distinguish HONGKAI-manufactured equipment, partner-integrated equipment and buyer-supplied items.
Common mistakes: A quotation calls the cable line a complete patch-cord factory but omits connectorization and optical testing. Another quotation lists a polishing machine but omits its connector fixtures, films, inspection adapter, reference cords or process responsibility.
أي خطوط HONGKAI تُشكّل الكابل الأساسي؟
For the reviewed simplex or duplex construction, the HONGKAI route uses the HK-30 to produce tight-buffered fiber and the HK-50 to apply aramid reinforcement and the outer jacket. If the factory purchases qualified tight-buffered fiber, the cable-making scope can start with the HK-50.
مرحلة التغليف الضيق HK-30
The reviewed HK-30 configuration receives optical fiber and applies the specified tight-buffer layer. Its functional modules include controlled payoff, preheating, material drying and feeding, extrusion, warm and cold cooling, online diameter measurement, capstan control and take-up. These functions define the production stage; the customer’s approved construction must define the actual polymer, color, dimensions, reel format and acceptance limits.
تم التحقق من مرجع HONGKAI HK-30 3D الذي يوضح خط إنتاج الغلاف المشدود الكامل. تظل قيم الأدوات النهائية والمواد وظروف التشغيل خاصة بكل مشروع.
مرحلة الهيكل والغلاف من HK-50 aramid
The reviewed HK-50 configuration receives the approved tight-buffered input, pays off the aramid reinforcement and extrudes the outer jacket. Its functional modules include input payoff, adjustable aramid payoff, positioning, material preparation, extrusion, cooling, online diameter measurement, capstan, accumulation and take-up.

Verified HONGKAI HK-50 3D reference showing the complete line used for an applicable aramid-reinforced simplex or duplex jacket stage. The accepted cable construction controls the final configuration.
The complete in-house route is therefore HK-30 tight buffering followed by HK-50 aramid reinforcement and jacketing. An HK-50-only route is appropriate when the factory has an approved external source for tight-buffered fiber and the incoming package, material, dimensions and optical condition match the signed HK-50 input specification.
The HK-30 and HK-50 documents are older project configurations. They verify the process stages and equipment functions, but their speeds, tensions, power, output, material options and package sizes must not be copied into a new proposal without reconfirmation.
The earlier HONGKAI شرح عملية كابل التوصيل also shows the HK-30 and HK-50 as separate production stages. Use it as orientation only; the approved cable drawing and current technical agreement control a new project.
How to verify: During FAT, connect the raw-fiber or tight-buffer input to the approved recipe and identify the resulting reel. Retain the actual cable drawing, material lots, tooling, dimensions, surface result, optical check and take-up package used for the trial.
ما هي العملية الكاملة للطرف الخلفي لكابل التوصيل LC أو SC؟
The supplied conventional LC/SC package covers cable cutting, jacket and buffer stripping, adhesive preparation and dispensing, connector assembly, crimping, curing, fiber scribing, polishing, end-face inspection, optical testing, labeling and packing. The ten powered back-end stations are integrated through HONGKAI’s specialist partner; connector-specific hand tools, fixtures and consumables complete the route.
The sequence below is a controlled planning route for the supplied epoxy-and-polish package. It is not a universal connector recipe. The approved connector-component instructions must set the exact strip dimensions, cleaning method, adhesive, assembly order, crimp tooling, cure cycle, polish sequence and optical limits. A factory should turn those instructions into a traveler or batch record before FAT.
1. Release the incoming cable and production order
Before cutting, verify the cable drawing, connector family, ferrule finish, finished length, quantity, label data and test requirements. Record the incoming reel or cable lot against the work order. If base cable is made in house, the released HK-50 reel is the handoff point; if it is purchased, the supplier’s reel identity and incoming inspection are the handoff evidence.
كيفية التحقق: يجب أن يكون المشغّل قادرًا على تتبع كل عينة FAT إلى بكرة كابل معتمدة واحدة، ودفعة مكونات موصل واحدة، ونسخة تعليمات عمل واحدة.
2. Cut the cable to controlled length
The automatic fiber cable cutting machine measures and cuts the released cable for the planned patch-cord length. The RFQ should define the cable-size range, required length range, tolerance, quantity count and whether allowance for stripping and connector assembly is included in the cutting instruction.
3D technical model based on the verified automatic cable cutting machine in Peter’s supplied conventional patch-cord package. Supplier branding has been removed; this back-end station is integrated through HONGKAI’s specialist partner.
فخ شائع: لا تعتمد فقط على طول القطع المعروض. أثناء اختبار القبول النهائي (FAT)، قم بقياس عينة محددة واحتفظ بكل من القيمة المضبوطة والنتائج الفعلية.
3. Strip the outer jacket
The optical cable stripping machine removes the required jacket length so the aramid yarn and buffered fiber can be prepared for the connector. The work instruction must match the actual simplex or duplex cable diameter, jacket material and connector boot or crimp sleeve. Acceptance should cover strip length, a clean cut and no damage to the reinforcement or buffered fiber.
3D technical model based on the verified outer-jacket stripping station. Supplier branding has been removed; final tooling is selected against the approved cable and connector construction.
4. Strip the tight buffer
The buffer stripping machine exposes the glass fiber to the dimension required by the connector assembly process. The operator must control the strip length and inspect the exposed fiber for coating residue, scratches or breakage. The machine does not replace cleaning and handling discipline.
3D technical model based on the verified tight-buffer stripping station in the supplied LC/SC package. Supplier branding has been removed.
ما الذي يجب أن تسأله: اطلب نطاق الكابل والغلاف المقبول، قائمة الشفرات أو أدوات الاستبدال، طريقة التحقق من طول التقشير ومعايير رفض الألياف التالفة.
5. Prepare adhesive with the Model 800 centrifuge
For the reviewed epoxy-and-polish route, the approved adhesive is prepared according to its supplier instruction. The Model 800 epoxy centrifuge supports controlled preparation and removal of entrained air before dispensing. Adhesive identity, mix ratio when applicable, preparation time, usable life, storage condition and disposal rule belong in the batch record.
3D technical model based on the verified epoxy centrifuge in the supplied package. Supplier markings have been removed; the approved connector and adhesive suppliers—not the image—define the preparation recipe.
المصيدة: قائمة ماكينات تقتصر على ذكر “إيبوكسي” فقط تترك المشتري دون نظام لاصق متوافق، أو تحكم في الدُفعات، أو قاعدة لعمر الاستخدام.
6. Dispense the adhesive
The epoxy dispenser delivers the prepared adhesive to the connector assembly process. The dispensing needle or adapter, dose, cleaning interval and confirmation method must suit the selected LC or SC connector components. Record the adhesive batch and preparation time with the work order.
3D technical model based on the verified adhesive dispensing station in the supplied conventional connector route. Supplier branding has been removed.
7. Insert the fiber, assemble components and crimp
The operator threads the prepared fiber into the ferrule, seats the cable and assembles the boot, crimp sleeve and other specified parts in the connector supplier’s approved order. The pneumatic crimping machine applies the connector-specific crimp through the correct die or fixture. The factory must provide stable compressed air at the agreed pressure and quality.
3D technical model based on the verified pneumatic crimping machine. Supplier branding has been removed; the connector construction controls the die, crimp position and acceptance check.
How to verify: Inspect component seating, aramid capture, boot position and crimp condition on representative LC and SC assemblies. Record the die or fixture identity and compressed-air condition used for FAT.
8. Cure the connector assembly
The curing oven stabilizes the adhesive under the approved time-and-temperature instruction. The work instruction must define loading orientation, fixture or holder, setpoint, actual cycle evidence, batch size and handling after cure. Do not transfer a cure recipe from another adhesive or connector system without approval.
3D technical model based on the verified connector curing unit in the supplied LC/SC package. Supplier branding has been removed.
الأدلة المطلوب طلبها: يجب أن يربط تقرير اختبار القبول النهائي (FAT) كل عينة بمجموعة المادة اللاصقة، وهوية الفرن، وسجل الدورة، والمشغّل المسؤول.
9. Scribe excess fiber and prepare the ferrule for polishing
After the approved cure and cooling sequence, use the specified fiber cutting pen or scribing tool to remove the protruding fiber without chipping the ferrule or damaging the fiber. Clean the connector and polishing fixture before loading. This is a hand-tool step in the supplied package, not a reason to invent another machine.
الأخطاء الشائعة: استخدام قوة زائدة أثناء الكتابة، وانتقال الحطام إلى تجهيزات التلميع، وعدم وجود قاعدة لاستبدال أدوات اليد البالية.
10. Polish the LC and SC ferrules
The fiber connector polishing machine performs the mechanical polishing stage. A complete station also needs the correct LC or SC holder, the approved UPC or APC process where applicable, polishing pads and films, cleaning materials and a controlled film-change rule. Peter’s supplied package lists connector-specific fixtures; they must be scheduled by actual launch product rather than assumed from the machine name.
3D technical model based on the verified polishing machine in the supplied package. Supplier branding has been removed; LC and SC require the correct connector-specific holder and approved consumable sequence.
What to ask: Require a connector-to-fixture matrix, film sequence, cleaning step, process ownership and replacement plan. A polishing machine without the right holder and consumables is not a working LC/SC station.
11. نظّف وافحص الوجه النهائي
After polishing, clean the connector with the approved materials and inspect it using the fiber connector inspection microscope with the correct adapter. The acceptance record should distinguish contamination that can be cleaned from scratches, chips or other defects that require rework or rejection.
3D نموذج تقني مبني على مجهر فحص الفيرول الموثّق في خلية العمل LC/SC الموردة. تمت إزالة علامة المورّد التجارية.
IEC 61300-3-35:2022 covers visual inspection and classification of contamination, scratches and defects on fibre-optic connector interfaces. The product specification still needs to identify the applicable connector interface, inspection method and acceptance criteria. Visual inspection does not replace finished-product optical testing.
12. Measure insertion loss and return loss with the 7420B
The 7420B insertion-loss and return-loss tester is the final powered test station in the supplied package. Before FAT, define fiber type, wavelength, reference method, connector adapters, reference cords, test direction, acceptance limits, calibration responsibility and how each result is tied to the finished patch cord.
3D technical model based on the verified optical tester in the supplied package. Supplier branding has been removed; the station supports traceable insertion-loss and return-loss testing of the finished conventional patch cord.
IEC 61300-3-4:2023 تتناول طرق قياس التوهين، بينما IEC 61300-3-6:2008 addresses return-loss measurement procedures. These references do not supply the product’s pass/fail values; those values must come from the approved product specification and customer agreement.
13. Perform final visual checks, label and pack
Use the visual fault locator when it belongs to the agreed work instruction, complete the final visual and dimensional checks, fit clean dust caps, apply the traceable label and pack the patch cord so the connector end faces and cable bend condition are protected. The released sample should carry the product code, length, connector configuration, fiber or cable identity, batch or serial reference and test status required by the buyer’s system.
The connector-processing area should be clean and have little airborne dust; a cleanroom is preferable when the product and quality requirements justify it. The layout must separate dirty preparation work from cleaned ferrules and finished connectors. The RFQ should assign compressed air, benches, lighting, cleaning materials, waste handling, labels and packaging instead of assuming they are included with the machines.
Pitfalls: The workcell depends on operator memory for strip length or polishing steps, end-face images are not tied to product identity, optical results have no documented reference method, or tested connectors are exposed to dust again before capping and packing.
ملخص معدات الطرف الخلفي
| Process stage | Reference equipment | التحكم المجاور المطلوب |
|---|---|---|
| Length cutting | ماكينة قطع الكابلات الأوتوماتيكية | السماحية الطولية، التسامح وقياس العينة |
| Jacket stripping | ماكينة تقشير الكابلات البصرية | أدوات الكابلات المحددة ومعايير الضرر |
| Buffer stripping | ماكينة تقشير الغلاف العازل الضيق | فحص وتنظيف حالة الألياف |
| Adhesive preparation | Model 800 | سجل هوية المادة اللاصقة، والخلطة، وفترة الصلاحية للاستخدام |
| Adhesive dispensing | Epoxy dispenser | الجرعة، المحول ووحدة التحكم في التنظيف |
| Connector crimping | ماكينة التثبيت الهوائية | قالب خاص بالموصل وهواء مضغوط |
| Curing | فرن معالجة الموصلات | تتبع الدورة والدفعة المعتمدة |
| Ferrule polishing | ماكينة تلميع وصلات الألياف | تثبيت LC/SC، والأغشية وتسلسل التنظيف |
| فحص الوجه النهائي | مجهر فحص وصلات الألياف | محول، معايير ونتيجة قابلة للتتبع |
| Optical testing | 7420B | الطول الموجي، الإعداد المرجعي، الحدود والمعايرة |
Which Fixtures, Tools and Consumables Belong in the RFQ?
Fixtures and consumables are part of the manufacturing system because they determine which connectors can be processed and whether the result is repeatable. A machine without the correct holder, film, adapter or cleaning control is not a complete station.
Peter’s supplied package names LC and SC polishing fixtures, including UPC and APC variants where applicable. FC and ST fixtures are also available in the reference package, but they should be added only when those connector families belong to the approved product list. The package also includes fiber and cable strippers, crimping pliers, aramid scissors, a fiber cutting pen, an electronic balance, adhesive, polishing pads and films, a visual fault locator and cleaning paper.
| Scope group | العناصر المقرر جدولتها | قرار المشتري |
|---|---|---|
| Connector fixtures | أ holders للتلميع، محولات الفحص، محولات الاختبار وأي قوالب تثبيت أو تجميع | اذكر كل عائلة موصل ونهاية الفيرول ومورّد المكونات |
| أدوات تحضير يدوية | أداة تقشير الألياف، أداة تقشير الغلاف، مقص الأراميد، أداة القطع وملقط التثبيت | حدد كمية الاستبدال، وتخصيص المشغل، وطريقة الفحص |
| Adhesive controls | أدوات لاصقة، أدوات وزن أو خلط، جهاز طرد مركزي، موزع، ومستلزمات تنظيف | تجميد نظام اللاصق المتوافق وضوابط التخزين والإعداد ومدة الصلاحية للاستخدام |
| Polishing consumables | وسادات، أفلام ومواد تنظيف | الموافقة على التسلسل، والدرجة، والمورّد، وقاعدة التغيير، ومراقبة الدُفعة |
| Test accessories | الحبال المرجعية، المحولات، القضبان الدليلية أو عناصر تكييف الوضع عند الحاجة، ومحدد العطل البصري | حدد طريقة الاختبار وواجهات الموصلات وملكية المعايرة |
| Finishing materials | أغطية الغبار، والملصقات، ومواد التغليف | حدد النظافة والهوية والعرض وحماية الشحن |
What to ask: Require a connector-to-fixture matrix and a consumable list for the launch products. The supplier should state which items are included, which wear out, which require regular replacement and which must be sourced from the connector or consumable manufacturer.
هل يجب على مصنع جديد شراء الكابل الأساسي أم تصنيعه داخليًا؟
Start with the narrowest complete route that can release the intended saleable patch cord. Buying qualified cable concentrates investment and training on connector assembly; adding HK-30 and HK-50 brings cable construction and supply control in house but also adds extrusion, material, reel and intermediate-quality responsibilities. The broader خريطة مسار إنتاج كابلات الألياف البصرية يساعد المشترين على وضع مسار الكابل الداخلي الضيق هذا بجانب عائلات خطوط الكابلات البصرية الأخرى دون اعتبار قائمة جهاز واحدة كقائمة عالمية.
| Decision factor | اشترِ كابلًا أساسيًا مؤهَّلًا | أضف إنتاج الكابلات الأساسية داخليًا |
|---|---|---|
| نطاق العملية الأولي | تأهيل الكابل الوارد بالإضافة إلى تجميع الموصل | معالجة الغلاف الضيق، والأراميد، والغلاف الخارجي بالإضافة إلى تجميع الموصل |
| التحكم في المورد الرئيسي | رسم الكابل، سجلات البكرة وإشعار التغيير | الألياف، المركبات، الأدوات، الوصفات، إمكانية تتبع الكابل أثناء المعالجة والبكرة |
| مهارات للتطوير | التحضير، تركيب الموصلات، التلميع، الفحص والاختبار البصري | جميع مهارات التجميع بالإضافة إلى البثق، والتبريد، والتوتر، والتحكم في الشد |
| Expansion constraint | محفظة الموردين المعتمدين وشروط مدة التوريد | نافذة المعدات المُوثَّقة، الأدوات، المواد وخطة التغيير |
| Handoff risk | موافقة البكرة الواردة إلى مسار التجميع | HK-30 output to HK-50, then finished reel to connector assembly |
Decision criterion: Compare the approved product mix, cable-source reliability, process knowledge, staffing, quality system and traceability burden. Do not justify the integrated route only with an unsupported production-volume or payback threshold.
Red flags: A proposal adds cable extrusion without an intermediate-reel release plan, or assumes that owning the cable line automatically reduces finished-patch-cord defects. Control improves only when materials, work instructions, operators and evidence are qualified together.
لماذا تم استبعاد MPO من مسار المعدات هذا؟
MPO is excluded because both its incoming multi-fiber cable and its connector-assembly workcell can differ from conventional single-fiber patch cords. A polishing fixture alone does not convert the ordinary patch-cord route into an MPO route.
The supplied specialist catalog separates the ordinary patch-cord machines from a dedicated MPO/MTP group. That group includes multi-fiber-specific preparation, polishing fixtures, curing, end-face or geometry inspection, polarity or channel control and multi-channel optical testing. Peter’s supplied experience also identifies more stable automatic polishing pressure as an important MPO consideration because one connector presents multiple fibers to the polishing process.
This article therefore stops at conventional single-fiber connector families. A separate MPO article must begin with the exact cable construction, fiber count, ferrule and connector system, polarity, end-face geometry requirement and channel-test method before selecting equipment.
Note: The supplied conversation mentions a project range of multiple fibers per MPO connector. That range remains a bounded project observation and will not be published as a universal MPO specification without Peter’s confirmation.
ما الذي يجب أن يثبته طلب عرض الأسعار (RFQ) واختبار القبول النهائي (FAT)؟
The RFQ must describe the complete route and responsibility boundary. FAT should use representative finished LC and SC patch cords from the approved launch range and prove them through the selected cable, connector, fixture, consumable, inspection and optical-test system.
| Acceptance layer | RFQ document | دليل FAT |
|---|---|---|
| المنتج النهائي | رسم الكابل، مكونات الموصل، نوع الألياف، الطول، التشطيب والملصق | العينة المحددة تطابق التكوين المعتمد |
| حدود المسؤولية | HONGKAI-manufactured, specialist-integrated, buyer-supplied and excluded-item matrix | كل محطة، ومرافق، واختبار له مالك وحالة بنود مفتوحة |
| الكابل الأساسي عند تضمينه | المواد، الأدوات، الوصفات، خطة التغليف والإصدار | بكرات ذات غلاف ضيق قابلة للتتبع وبكرات الكابلات الجاهزة مع سجلات الأبعاد والخصائص البصرية المتفق عليها |
| Cable preparation | تعليمات العمل للقطع والتعرية | الطول المقيس، وحالة الطرف المُحضَّر، وهوية المسافر |
| Connector assembly | المكون، اللاصق، تعليمات التثبيت والمعالجة | دفعات المكونات والمستهلكات، والإعدادات وسجل الدورة |
| Polish and inspection | مصفوفة الموصل إلى التجهيزات، تسلسل الفيلم ومعايير الفحص | Traceable end-face result for each FAT sample |
| Optical test | الطول الموجي، إعداد المرجع، الحدود، الاتجاه والعينة | Recorded insertion-loss and return-loss results when required |
| Work environment | مستوى النظافة، التحكم في الغبار، الهواء المضغوط وظروف طاولة العمل | منطقة الخلفية نظيفة، ومنخفضة في الغبار المحمول جواً ومناسبة لعملية الموصل المتفق عليها |
| Packing and labels | أغطية الغبار، حقول الملصقات، طريقة التغليف والمورّد المسؤول | Released sample has the agreed identity, protection and presentation |
| Handover and training | التخطيط، المرافق، الكتيبات، المعايرة، قطع الغيار، المواد الاستهلاكية وتقسيم التدريب | HONGKAI trains operators on HONGKAI equipment; the integration partner trains operators on partner equipment |
قائمة المراجعة:
- ☐ Launch products and connector families are listed separately
- ☐ نطاقات تصنيع الكابلات وتجميع الموصلات منفصلة
- ☐ Every machine, fixture, adapter and consumable has a named product purpose
- ☐ HONGKAI-manufactured, specialist-integrated and buyer-supplied items are explicit
- ☐ مكونات الألياف الواردة، والكابلات، والموصلات، والمستهلكات تخضع لقواعد الموافقة
- ☐ End-face inspection and optical testing are both included where required
- ☐ FAT samples use the agreed cable, connectors, fixtures and work instructions
- ☐ منطقة الخلفية، والهواء المضغوط، والتغليف والملصقات لها مالكون معينون
- ☐ Training, calibration, maintenance and traceability ownership are assigned
Evidence to request: Keep the approved drawings, equipment configuration, material and component lots, work instructions, operator identity, settings, cure and polish records, inspection images, optical-test setup, raw results, sample labels and a dated open-item list. The separate دليل تركيب وتشغيل خط الألياف البصرية provides a broader acceptance framework for utilities, documentation, startup and handover.
Note: The complete patch-cord production route is the smallest connected system that can turn approved inputs into a repeatable, traceable finished product. Equipment count alone does not prove that the route is complete.
