


A wire bunching machine should be selected from the finished conductor backward, not from a reel size or maximum-speed headline. A factory owner or technical buyer must first define what enters the machine, what conductor must leave it, how that conductor will be tested, and which package must connect to the next process.
The correct wire bunching machine is the smallest project configuration that can produce the approved conductor across its required wire range, lay window and reel interface while maintaining controllable tension and measurable acceptance evidence. Nominal speed does not prove that the conductor will remain stable from an empty to a full take-up reel. The RFQ should therefore define the input wires, finished conductor, lay direction, packages, control functions, safeguards and FAT samples before a model is approved. HONGKAI can map those inputs to a machine family, but final performance must be confirmed against the exact cable and project conditions.
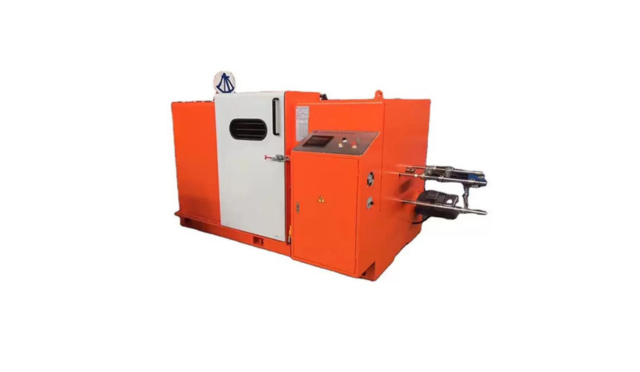
Tham khảo máy bện dây thật của HONGKAI. Máy bện cỡ nhỏ hơn này được hiển thị để phục vụ thảo luận lựa chọn; model chính xác, cách bố trí đầu vào và phạm vi cung cấp vẫn phải được xác nhận trong đặc tả dự án.
This guide is for low-voltage cable factory owners, production managers and technical procurement teams. It does not treat bunching, ordered stranding and cable laying-up as interchangeable names. The buyer’s decision is whether a proposed buncher matches one approved conductor design and whether the supplier can prove that match before shipment.
What Must Buyers Define Before Selecting a Wire Bunching Machine?
Người mua cần cố định tám quyết định liên quan trước khi lựa chọn máy bện dây: dây dẫn thành phẩm, dây đầu vào, tiêu chuẩn sản phẩm áp dụng, khoảng bước xoắn, giao diện cuộn dây, phương pháp điều chỉnh lực căng, hệ thống an toàn và bằng chứng nghiệm thu tại xưởng (FAT). Mỗi quyết định này đều làm thay đổi cấu hình máy khả dụng và các bằng chứng cần thiết khi nghiệm thu. Một danh mục sản phẩm đa dạng rất hữu ích cho việc sàng lọc ban đầu, nhưng không thể thay thế bản vẽ dây dẫn đã được phê duyệt và kế hoạch mẫu. Nhà cung cấp cần có đầy đủ định nghĩa về đầu vào và đầu ra trước khi xác nhận model máy hoặc điều kiện sản xuất ổn định.
1. Finished Conductor: Which conductor must the machine produce?
Why it matters: The finished conductor is the selection anchor. Nominal cross-sectional area alone does not state whether the conductor is bunched, concentrically stranded, compacted, flexible, coated, insulated or made to a special construction. Two conductors with the same nominal area can require different individual-wire counts, wire diameters, lay behavior, tension and downstream handling. A supplier cannot responsibly select a wire bunching machine from a cable name such as “flexible wire” without the approved construction.
What to ask: Send the finished-conductor drawing or specification with material, nominal area, construction class or product-standard reference, individual-wire count and diameter, finished diameter where controlled, coating or plating, direction, lay requirement, joint policy and downstream process. State whether the buncher receives bare wires, coated wires or already insulated cores. Mark every range as required, optional or future instead of combining unrelated products into one maximum envelope.
How to verify: Compare the supplier’s proposed operating window with every approved conductor at its smallest and largest required condition. Require the quotation to show which inputs were used to select the machine and which products remain outside the scope. IEC 60228:2023 covers nominal cross-sectional areas, wire numbers and sizes, and resistance values for several conductor types in power cables and cords, but the applicable finished-cable standard still decides whether IEC 60228 applies to the product.1
Red flags: The proposal lists only finished cable diameter, treats a conductor class as a machine model, assumes that all fine-wire conductors use the same process, or includes compacted and non-compacted constructions without separate tooling and acceptance review.
Use the individual-wire material, diameter and count together with the finished outside diameter, required lay and finished-product characteristics to decide whether a buncher, cage strander or another stranding system is appropriate. The route remains product-specific rather than being fixed by nominal conductor area or a generic cable name.
2. Input Wires: Are the material, diameter, count and condition complete?
Why it matters: A wire bunching machine handles individual inputs before it creates the finished bundle. Their material, diameter, count, surface, coating, hardness, incoming package and tension condition affect routing, guide contact, wire-break detection and the usable operating window. A machine that accepts the final nominal area on paper may still be unsuitable for the actual individual wires or packages.
What to ask: Define conductor material and coating, individual-wire diameter range, exact wire count for each product, incoming spool dimensions, flange and barrel condition, maximum approved package mass, payoff arrangement, allowable joints, surface cleanliness and any sensitivity to scratching or deformation. Identify whether the factory will buy prepared wire or draw, anneal or tin it on site. State the expected variation from upstream production rather than giving only a nominal value.
How to verify: Inspect the complete material path from every payoff position through guides and wire-break devices into the bunching zone. During FAT, use the agreed incoming packages and representative wires rather than substitute material chosen only because it runs easily. Confirm that guides, contact points and detection devices are suitable for the defined wire surface and that an input fault can be identified without damaging the retained conductor.
Red flags: The supplier selects a buncher from finished area only, the proposed payoff cannot accept the buyer’s actual spools, input wire count is described as “about” a value, or the FAT plan allows different wire material and package geometry from production.
Treat a proposal as preliminary when the conductor material, individual-wire diameter before bunching, wire count, finished outside diameter or required finished characteristics is missing, even if the nominal cross-sectional area is already known.
3. Acceptance Basis: Which standard and finished tests control approval?
Why it matters: The wire bunching machine creates geometry, but the factory sells a conductor or cable that must meet an approved product specification. A visually uniform bundle does not prove conductor resistance, construction, dimensions or suitability for the next process. The buyer must separate machine functions from finished-product acceptance and name who supplies each test method and instrument.
What to ask: Identify the finished-cable standard, conductor clause, customer drawing and factory control plan that apply. State which properties are checked at the bunching stage and which are verified only after insulation or final cable production. Define sample conditioning, measurement temperature where relevant, instrument responsibility, pass/fail limits, record format and disposition of material made during setup or adjustment.
How to verify: Build an acceptance matrix that connects each requirement to a sample, test method, instrument, responsible party and retained record. If IEC 60228 applies, confirm the exact conductor type and edition rather than citing the standard as a general quality badge. The IEC publication record notes that its requirements generally relate to conductors in finished cable, so an intermediate bunching check must be connected to the finished-product control plan instead of being presented as automatic compliance.1
Red flags: The quotation says only “according to IEC,” a resistance result has no sample temperature or method, the FAT checks appearance but not the agreed conductor properties, or the supplier promises certification that neither the machine nor the FAT can establish.
4. Lay Window: Which lay length and direction must remain stable?
Why it matters: Lay length is a product setting, not a decorative parameter in a catalog table. The required window, S or Z direction, wire construction, speed and tension interact. A very wide nominal range is not useful if the machine cannot produce the buyer’s actual conductor with stable lay and acceptable handling under the agreed production condition.
What to ask: List every required lay length or approved range by conductor, the lay direction, tolerance and measurement method. Define whether settings change through gears, electronic control or another mechanism, and include the supplied change parts in the scope. Ask the supplier to state any speed, package or conductor condition that limits the requested lay window rather than quoting one universal maximum.
How to verify: First compare the requested lay with the pitch table for the exact proposed machine. A value inside that table is only a candidate setting, so measure actual lay on agreed FAT samples after the machine reaches the test condition and repeat at more than one take-up state when the project risk justifies it. Record the recipe or gear combination, direction, line state, sample identity and result. One Φ800 configuration reviewed in HONGKAI’s local material uses interchangeable pitch gears and supports S or Z operation; that is a configuration example, not proof that every HONGKAI wire bunching machine uses the same mechanism or range.
Red flags: The supplier lists lay length without direction or tolerance, substitutes calculated pitch for measured conductor evidence, omits change gears or recipes from the supply, or promises the same stable speed at every lay and conductor condition.
A requested lay outside the exact machine table should remain outside scope unless a revised configuration and new product evidence are agreed. During FAT, compare the set value with the actual conductor by counting or measuring lays over a known sample length using the approved method.
5. Reel Interface: Do the payoff and take-up packages fit factory flow?
Why it matters: Reel diameter is only one interface. Flange condition, barrel diameter, traverse width, center hole, loading method, package mass, lifting access, traverse control and downstream handling decide whether the machine can be used safely and efficiently. A reel mismatch can delay commissioning even when the bunching head itself is suitable.
What to ask: Supply drawings or verified dimensions for every incoming and outgoing package, including tolerances and maximum approved mass. Define shafted or shaftless loading, lifting method, reel clamping, traverse range, loading aisle, finished package build and transfer to the next process. Confirm whether the supplied reel is a machine reel, shipping reel or production package and whether adapters are included.
How to verify: Load the agreed reels during FAT or perform a dimensional and functional interface check when production reels cannot be shipped. Run traverse across the usable width, inspect edge build and confirm that lifting, clamping, braking and removal can be completed by the approved method. Check the factory layout for actual reel movement and service access instead of assuming that machine footprint alone proves fit.
Red flags: A proposal says “800 mm reel” without a drawing, the flange fits but the center hole or traverse width does not, hydraulic lifting is listed without load and interface confirmation, or the buyer discovers after delivery that production reels cannot pass through the access route.
Confirm the dimensions of every payoff and take-up position before the machine is finalized, whether the arrangement uses one reel or several. Send any custom package to the supplier early enough to verify or modify the loading, clamping and traverse interfaces. For empty-to-full tension checks, retain the machine display record when available; otherwise agree a controlled manual or mechanical measurement method instead of relying on visual judgment.
6. Tension Control: How will the conductor remain stable from empty to full reel?
Why it matters: Take-up diameter changes during production, so the control system must manage tension as the package builds. Excess tension can deform or stretch fine wires; insufficient or unstable tension can disturb the bundle, traverse and downstream payoff. A named controller or magnetic-powder device is not evidence until the complete control behavior is demonstrated with the agreed conductor.
What to ask: Request the tension-control principle, sensing or feedback method, adjustment range, empty-to-full compensation, startup and slowdown behavior, recipe control, alarm conditions and operator permissions. Define how upstream payoff tension and downstream take-up tension are coordinated. Ask what evidence will show that adjustment can be made safely and that a wire break or abnormal condition does not leave uncontrolled stored motion.
How to verify: Observe startup, steady running, speed change, controlled stop and representative package build. Retain the operating settings and inspect the conductor, lay, reel build and any tension record available from the system. A local Φ800 reference configuration reviewed by HONGKAI uses PLC tracking with magnetic-powder take-up tension; the project still needs conductor-specific FAT evidence before that control concept can be accepted.
Red flags: The supplier describes tension as “automatic” without a control explanation, FAT starts with a partly filled reel only, operators can overwrite settings without control, or the machine remains running after an input-wire break.
7. Safety Controls: Which hazards and automatic stops must be verified?
Why it matters: High-speed rotating equipment, moving reels, stored tension and electrical systems create hazards that must be addressed by the machine design, factory risk assessment and operating controls. A closed cover or emergency-stop button alone does not prove that all hazards are controlled. The acceptance plan should verify the safeguards supplied with the exact configuration and the interfaces that remain the buyer’s responsibility.
What to ask: Require a machine-specific risk and safeguard review, guarding and interlock description, emergency-stop functions, wire-break and door-open behavior, braking method, safe reel-loading procedure, isolation points, warning labels and required factory utilities. Define the stopping and restart sequence after each protective event. State who supplies external fencing, lifting devices, compressed air, foundations and site electrical protection where applicable.
How to verify: Test agreed protective functions during FAT without bypassing safeguards. Confirm that the final electrical documentation matches the supplied machine and that faults require an intentional, controlled reset. IEC 60204-1:2016 with Amendment 1:2021 applies to electrical, electronic and programmable electronic equipment of machines from the supply connection, while ISO 12100:2010 provides risk-assessment and risk-reduction principles.23
Red flags: A safety door is shown but not interlocked, a stop test is skipped because it interrupts production, braking behavior is not defined, or the proposal uses a standard number as a certification claim without project-specific evidence.
8. FAT Evidence: Which sample and records prove the machine is acceptable?
Why it matters: A no-load rotation test proves assembly and basic control only. The buyer needs evidence that the wire bunching machine can handle representative inputs, produce the agreed lay and package, respond to faults and transfer usable conductor to the next stage. FAT should be designed before the order so the supplier can prepare material, reels, tooling and test instruments.
What to ask: Define the FAT conductor or conductor family, input wire, package state, lay, direction, run condition, sampling points, measured properties, safeguards to test, documents to review and treatment of open items. Include the expected recipe, tooling and change parts in the record. Separate witness tests from supplier pre-tests and state which raw results, photographs, videos and sample lengths the buyer receives.
How to verify: Trace one sample from identified input reels through the machine settings to the finished reel and retained test record. Compare the actual supplied machine, nameplates, drawings, software or recipe version, spares and tooling with the signed scope. Repeat a setting change or fault recovery when it is material to production, then confirm that the resulting conductor still meets the agreed acceptance basis.
Red flags: FAT uses unidentified material, the accepted conductor differs from the buyer’s smallest or most demanding product without written rationale, only a short edited video is retained, or deviations are closed verbally without owner, date and verification evidence.
Decision criterion: Choose the FAT conductor from the confirmed finished outside diameter and requested lay, including the operating condition that makes the agreed lay-and-speed combination most demanding. Check the machine setting against the actual sample over a known length. A matching result demonstrates the pitch condition for that sample only; it does not prove an untested conductor or speed.
Note: A buncher is ready for selection only when its input, output, package, control and acceptance boundaries can all be written into the same project specification.
How Should a Buyer Compare Wire Bunching Machine Models?
Wire bunching machine models should be compared by required operating overlap, not by choosing the largest reel or fastest catalog value. The usable model must cover the individual wires, finished conductor, lay window and package interfaces at the same time. Controls, safeguards, change parts, access and downstream handling then decide whether that mechanical range is practical. HONGKAI’s current product family is a screening reference; the signed project specification must remain the final authority.
Hiện tại HONGKAI wire bunching machine page presents several model sizes from HK-300 through HK-1250. Its table changes input range, finished-conductor range, lay range, reel, rotational speed, drive and machine dimensions by model. Buyers should use that page to identify candidates, then require a returned selection matrix based on the actual conductor list.
| Câu hỏi so sánh | Bằng chứng do người mua cung cấp | Bằng chứng do nhà cung cấp trả về |
|---|---|---|
| Mô hình có chấp nhận từng dây cáp yêu cầu không? | Vật liệu, lớp phủ, đường kính, số lượng và bao bì đầu vào theo sản phẩm | Cửa sổ đầu vào khả dụng và các điều kiện loại trừ |
| Mô hình có thể sản xuất mọi dây dẫn được phê duyệt không? | Cấu trúc, diện tích hoàn thiện, kích thước, bước xoắn và tiêu chuẩn | Mô hình đã chọn, dụng cụ và bản đồ ánh xạ theo sản phẩm |
| Chiều dài bước xoắn yêu cầu có thực tế không? | Lay values, direction, tolerance and measurement method | Setting method, change parts and limiting conditions |
| Do packages connect to the factory? | Payoff and take-up drawings, mass and handling route | Reel interfaces, adapters, traverse and loading method |
| Can controls manage the production state? | Product mix, changeover and operator constraints | Tension concept, recipes, alarms and permissions |
| Can the scope be accepted? | FAT samples, tests, instruments and records | Pre-test plan, witness plan and deviation process |
A larger machine is not automatically a safer investment. It can change floor space, rotating mass, package handling, access, utilities and the economics of smaller products. A smaller machine is not automatically more efficient if it excludes a planned conductor or requires frequent transfer to another process. The buyer should compare the approved present range and one realistic future range, then label every other possibility as outside scope.
A local Φ800 HONGKAI reference configuration includes a Siemens PLC, Weinview touchscreen, magnetic-powder take-up tension, electromagnetic braking, oil-pump reel lifting, wire-break and door-open stops, digital length measurement, interchangeable pitch gears and a defined spare-tool set. Those functions are useful RFQ prompts. They are not a universal HONGKAI specification, and every brand, range, power value, reel dimension and control function must be reissued for the selected project.
A dedicated smaller machine should be evaluated when the confirmed product uses finer wires outside the practical range of a larger candidate. A broader-range machine is justified only when a named future conductor maps its material, individual wires, finished diameter, lay and reels to a verified machine window. “Future expansion” without that product definition is not a reason to buy unused range.
The final comparison should therefore show where the buyer’s products overlap with the proposed model and where they do not. Any claimed future capability should be tied to a named conductor, tooling set, package and test plan. “Expandable” without those details is not an engineering boundary.
Note: Model size is a consequence of the approved conductor portfolio, not the first decision in the selection process.
What Should the RFQ and FAT Require Before a Wire Bunching Machine Is Approved?
A complete RFQ should allow the supplier to select a wire bunching machine without guessing, and a complete FAT plan should prove the returned configuration without changing the acceptance basis. The buyer should attach product, input-wire, reel, layout, utility, control and test data in one controlled package. The supplier should return a model-selection matrix, complete scope, exclusions, drawings, control description and sample plan. Approval should remain pending until unresolved technical assumptions are converted into signed requirements or clearly excluded conditions.
- ☐ Approved finished-conductor drawing and applicable cable standard
- ☐ Individual-wire material, coating, diameter, count and variation
- ☐ Diện tích dây dẫn hoàn thiện, cấu trúc, kích thước và cơ sở điện trở
- ☐ Chiều dài bước xoắn yêu cầu, dung sai, hướng và phương pháp đo
- ☐ Bản vẽ cuộn đầu vào và đầu ra, khối lượng bao bì và phương pháp xếp tải
- ☐ Phạm vi cấp dây, phương pháp căng, phát hiện đứt dây và bố trí hướng dẫn
- ☐ Khái niệm căng cuộn thu, di chuyển ngang, hành vi từ rỗng đến đầy và công thức
- ☐ Các bánh răng thay thế, dụng cụ, bộ chuyển đổi và cuộn sản xuất được cung cấp
- ☐ Thông tin về bảo vệ, liên động, dừng khẩn cấp, phanh và cách ly
- ☐ Nguồn điện, khí nén, tải sàn, không gian tiếp cận và giới hạn nâng
- ☐ Các cấp điều khiển người vận hành, cảnh báo, lịch sử sự cố và trách nhiệm sao lưu
- ☐ FAT vật liệu, danh tính mẫu, điều kiện chạy và điểm chứng kiến
- ☐ Bằng chứng về việc chấp nhận về bố trí, kích thước, điện trở và xử lý downstream
- ☐ Kiểm tra chức năng bảo vệ và phục hồi sự cố được kiểm soát
- ☐ Bản vẽ cơ khí, điện và tiện ích phù hợp với bản sửa đổi đã cung cấp
- ☐ Công cụ, phụ tùng thay thế, hướng dẫn, công thức và đào tạo nằm trong phạm vi
- ☐ Các lệch chuẩn, loại trừ và sản phẩm tương lai với chủ sở hữu chịu trách nhiệm
Trước khi ban hành, người mua nên loại bỏ các phạm vi mâu thuẫn và tách riêng các sản phẩm hiện tại khỏi các sản phẩm tiềm năng trong tương lai. Một thông số kỹ thuật không nên yêu cầu đồng thời sản phẩm dây mảnh nhỏ nhất, dây dẫn lớn nhất trong tương lai và tốc độ tối đa, trừ khi dự án thực sự cần sự kết hợp đó và nhà cung cấp có thể kiểm tra được. Nếu có nhiều hơn một họ máy là hợp lý về mặt kỹ thuật, hãy yêu cầu sự đánh đổi về gói thiết bị, không gian sàn, thời gian chuyển đổi, cửa sổ vận hành ổn định và bằng chứng, thay vì yêu cầu một khuyến nghị duy nhất không được giải thích.
Tại FAT, bắt đầu bằng việc xác định danh tính. Xác minh mô hình máy, các thành phần được cung cấp, bản vẽ, lưới bảo vệ, phiên bản điều khiển, dụng cụ và cuộn dây so với phạm vi đã ký. Sau đó, truy vết dây dẫn đã đồng thuận từ các gói đầu vào đã xác định thông qua các thiết lập và chức năng bảo vệ đến cuộn dây hoàn thiện. Giữ lại các bản ghi đo lường thô và các mục chưa giải quyết, không chỉ là một video quảng bá.
Giao diện ở giai đoạn tiếp theo là một phần của việc chấp nhận. Một dây dẫn có thể vượt qua kiểm tra ngoại quan ở giai đoạn xoắn nhưng vẫn gây ra sự cố trong quá trình đùn hoặc cáp nếu cấu trúc cuộn, hành vi đầu ra, bề mặt hoặc lịch sử lực căng không phù hợp. Khi có thể, hãy giữ lại đủ dây dẫn đã xác định để xác minh downstream hoặc thống nhất một phương pháp cụ thể cho dự án. Việc phát hành cáp cuối cùng vẫn tuân theo kế hoạch kiểm soát sản phẩm hoàn thiện đã được phê duyệt.
Nếu nhà máy đang so sánh một tuyến sản xuất cáp hạ áp hoàn chỉnh thay vì một máy đơn lẻ, hãy sử dụng HONGKAI hướng dẫn lựa chọn tuyến sản xuất cáp hạ áp để ánh xạ các bước chuẩn bị dây dẫn, xoắn, cách điện, cáp, bảo vệ điều kiện, bao bọc, kiểm tra và xử lý. Máy xoắn dây chỉ nên được đưa vào tuyến này khi cấu trúc dây dẫn đã được phê duyệt yêu cầu nó.
Lưu ý: Quyết định mua hàng là có thể kiểm toán khi một kỹ sư khác có thể tái tạo lại lý do chọn mô hình, sản phẩm mà nó phải tạo ra, cách thức kiểm tra và điều kiện nào nằm ngoài phạm vi.
-
IEC 60228:2023, Dây dẫn của cáp cách điện. Bản ghi chính thức IEC bao gồm các diện tích tiết diện danh định, số lượng và kích thước dây, và giá trị điện trở cho một số loại dây dẫn trong cáp và dây điện; tính ứng dụng phụ thuộc vào tiêu chuẩn cáp.↩ ↩
-
IEC 60204-1:2016, An toàn máy móc — Thiết bị điện của máy móc — Phần 1, với Sửa đổi 1:2021 available từ bản ghi xuất bản IEC. Nó bao gồm thiết bị điện, điện tử và điện tử có thể lập trình của máy từ điểm kết nối nguồn.↩
-
ISO 12100:2010, An toàn máy móc — Nguyên tắc chung về thiết kế — Đánh giá và giảm thiểu rủi ro. ISO nêu rằng tiêu chuẩn này đã được xem xét và xác nhận lần cuối vào 2022 trong khi một bản sửa đổi vẫn đang được phát triển.↩



