


കേബിൾ ഉൽപ്പാദന മാനേജർക്ക് കേബിൾ വലിപ്പം മാറ്റിയതിന് ശേഷവും, ഒരു ലെയർ ചേർത്തതിന് ശേഷവും അല്ലെങ്കിൽ അസമമായ ഇൻസുലേഷൻ കണ്ടെത്തിയാലും പുതിയ ടൂളിംഗ് ആവശ്യമായി വരാം. പുതിയ ക്രോസ്ഹെഡ് ഓർഡർ ചെയ്യുന്നതിന് മുമ്പ്, കേബിൾ ആവശ്യകതയെ ഇൻസ്റ്റാൾ ചെയ്ത ടൂളിംഗിന്റെ അവസ്ഥയിൽ നിന്നും ലൈനിന്റെ പ്രവർത്തനരീതിയിൽ നിന്നും വേർതിരിക്കുക.
ഒരു പുതിയ കേബിൾ വലിപ്പത്തിന് എല്ലായ്പ്പോഴും ഒരു പുതിയ ക്രോസ്ഹെഡ് ആവശ്യമില്ല. വരുന്ന കോർ ഘടന, ആവശ്യമായ ബാഹ്യ ആകൃതിയും വലിപ്പവും, ഹെഡിന്റെ സ്ഥിരീകരിച്ച പരിധി എന്നിവ പരിശോധിക്കുക. തുടർന്ന് ലൈൻ അലൈൻമെന്റ്, വാൾ കനം, ഹീറ്റിംഗ് എന്നിവ പരിശോധിക്കുക: ടൂളുകൾ മാറ്റുകയോ ഹെഡ് ക്രമീകരിക്കുകയോ ചെയ്താൽ മതിലിന്റെ അസമമായ കനത്തിന്റെ എല്ലാ കാരണങ്ങളും പരിഹരിക്കാൻ കഴിയില്ല.
ഈ ഗൈഡ് ഇൻസുലേഷനും ജാക്കറ്റ് എക്സ്ട്രൂഷനുമായി ബന്ധപ്പെട്ട വിവരങ്ങളെയും തെളിവുകളെയും കുറിച്ചാണ്. ഇത് ഒരു സാർവത്രിക ഡൈ-സൈസിംഗ് പാചകക്കുറിപ്പോ, ഒരു പ്രത്യേക മെഷീനിനായുള്ള സെന്ററിംഗ് നടപടിയോ, അതിന്റെ ഓപ്പറേറ്റിംഗ് മാനുവലിന് പകരമാവുന്നതോ അല്ല.
അപേക്ഷിക്കുന്ന ലെയറിൽ നിന്ന് ആരംഭിക്കുക
ക്രോസ്ഹെഡിലേക്ക് പ്രവേശിക്കുന്ന ഉൽപ്പന്നത്തിന്റെയും അതിൽ നിന്ന് പുറത്തേക്ക് പോകുന്ന ഉൽപ്പന്നത്തിന്റെയും ഒരു ഡ്രോയിംഗ് കൊണ്ട് ആരംഭിക്കുക. സോളിഡ് കണ്ടക്ടർ, സ്ട്രാൻഡഡ് കണ്ടക്ടർ, അസംബ്ലഡ് കേബിൾ കോർ എന്നിവയുടെ നോമിനൽ വ്യാസങ്ങൾ സമാനമാണെന്നതിനാൽ മാത്രം അവയെ പരസ്പരം കൈമാറാവുന്ന ഇൻപുട്ടുകളായി കണക്കാക്കരുത്.
Record the incoming construction, its size range and the layer being applied. For a finished cable, identify whether the purchase concerns conductor insulation, an inner sheath or the outer jacket. Where several materials or layers are involved, identify them separately rather than requesting a generic “multilayer head.”
ഇവ ഉൾപ്പെടുത്തി ഒരു ചെറിയ ഉൽപ്പന്ന രേഖ തയ്യാറാക്കുക:
- ഇൻകമിംഗ് കണ്ടക്ടർ അല്ലെങ്കിൽ കോർ ഡ്രോയിംഗും പ്രതിനിധി സാമ്പിളുകളും.
- കോമ്പൗണ്ട് നിർമ്മാതാവ്, കൃത്യമായ ഗ്രേഡ്, പ്രോസസ്സിംഗ് മാർഗനിർദ്ദേശങ്ങൾ.
- ആവശ്യമായ ചുമരിന്റെ കനം, പൂർത്തിയാക്കിയ ബാഹ്യ അളവ്, ബാധകമായ സ്വീകാര്യതാ പരിധികൾ.
- ഏതെങ്കിലും സ്ട്രൈപ്പ് അല്ലെങ്കിൽ മറ്റ് പ്രത്യേക മെറ്റീരിയൽ ഫീഡ് ഉൾപ്പെടെയുള്ള ലെയറുകളുടെ എണ്ണവും ക്രമവും.
- കേബിൾ സ്പെസിഫിക്കേഷനിൽ ഉൾപ്പെടുത്തിയിട്ടുണ്ടെങ്കിൽ, സ്ട്രിപ്പിംഗ്, ആധേഷൻ അല്ലെങ്കിൽ ലെയർ സെപ്പറേഷൻ എന്നിവയ്ക്കുള്ള ബാധകമായ ആവശ്യങ്ങൾ.
- നിലവിലെ എക്സ്ട്രൂഡർ, ക്രോസ്ഹെഡ് ഐഡന്റിറ്റി, ലൈൻ ലേഔട്ട്, പ്രസ്താവിച്ച ഓപ്പറേറ്റിംഗ് റേഞ്ച് എന്നിവ.
എക്സ്ട്രൂഷൻ രീതിയും ലെയർ ക്രമീകരണവും പ്രത്യേകം തിരഞ്ഞെടുക്കുക
Pressure tooling and tubing tooling describe different extrusion approaches. Single-layer and coextrusion describe the layer arrangement. These are separate decisions, not four competing names for the same choice. Tooling manufacturers offer different pressure/tubing, layer and centering configurations.1
Start with the product and required wall thickness when choosing the extrusion approach. In the HONGKAI applications discussed for this guide, the optical-fiber tube operation uses tubing tooling, while the sheath operation uses pressure tooling. These are application examples, not a rule that every optical cable tube or jacket uses the same method.
Next, specify whether the product needs one layer, two layers in separate operations, or two layers extruded together. If both layers must be applied in one pass, the proposed head and material feeds must support that coextrusion arrangement. Identify a color stripe separately; a stripe is not automatically another complete sheath layer.
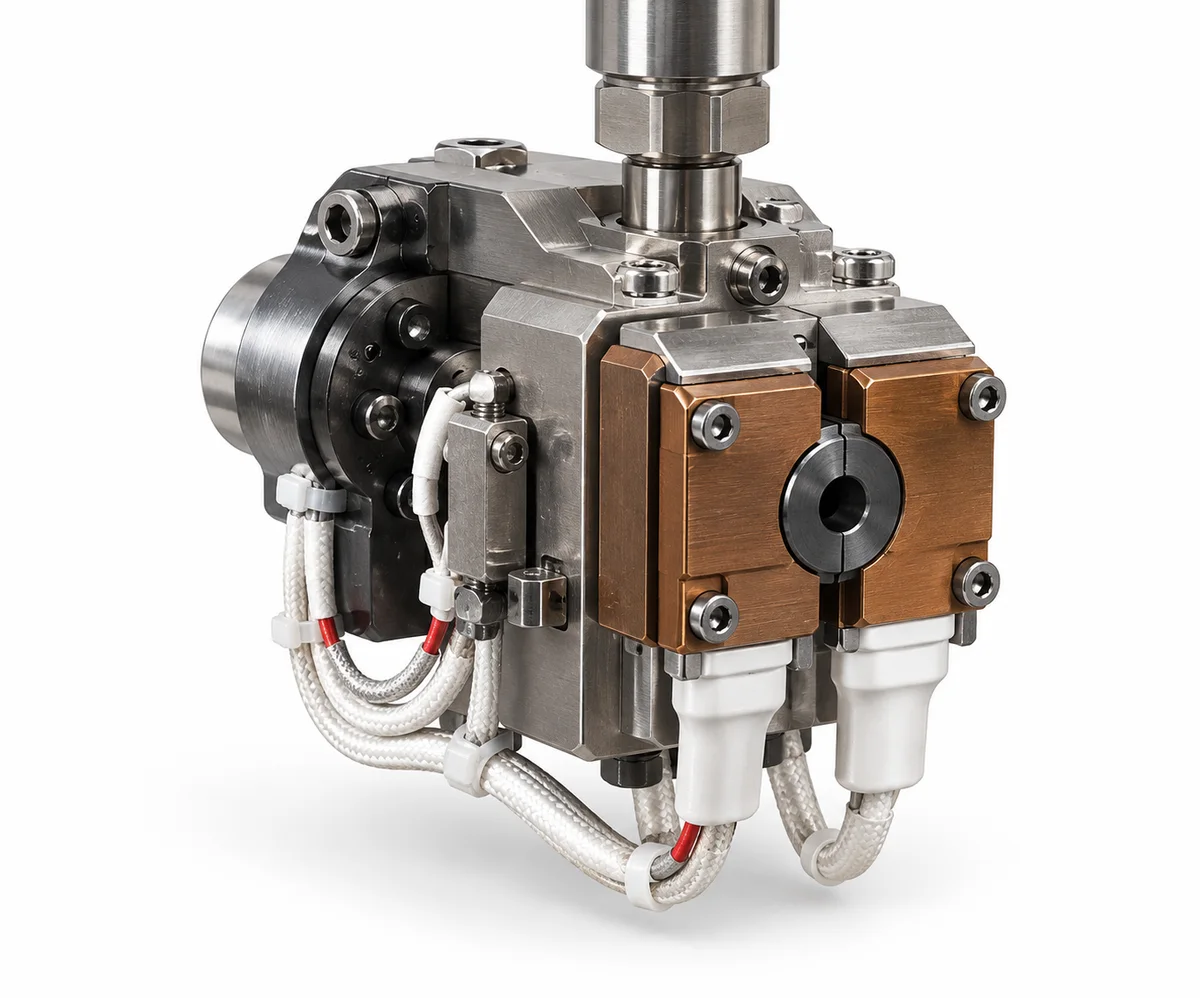
HONGKAI 3D ഇരട്ട-ലെയർ കോഎക്സ്ട്രൂഷൻ ക്രോസ്ഹെഡിന്റെ ബാഹ്യ റഫറൻസ്, ഒരു നിറ-വരി അടുക്കുള്ളത്. ഇത് അളവുകൾ നൽകിയ ഡ്രോയിംഗോ മറ്റ് ക്രോസ്ഹെഡുകൾക്കുള്ള സാർവത്രിക രൂപകൽപ്പനയോ അല്ല.
For an expansion project, separate the first approved product from future products. Ask the supplier to identify which changes remain within the proposed head and tooling range, and which require a different setup or an application trial. A possible future configuration should not be listed as proven production scope.
ഉപകരണങ്ങൾ മാറ്റുകയോ അല്ലെങ്കിൽ മുഴുവൻ ക്രോസ്ഹെഡും മാറ്റുകയോ?
Check the tip when the incoming core construction changes, and the die when the required outside shape or dimension changes. If the product is outside the installed head’s confirmed size range, a tooling change alone is not enough: the head must also change. Staying within that range is only the first compatibility check.
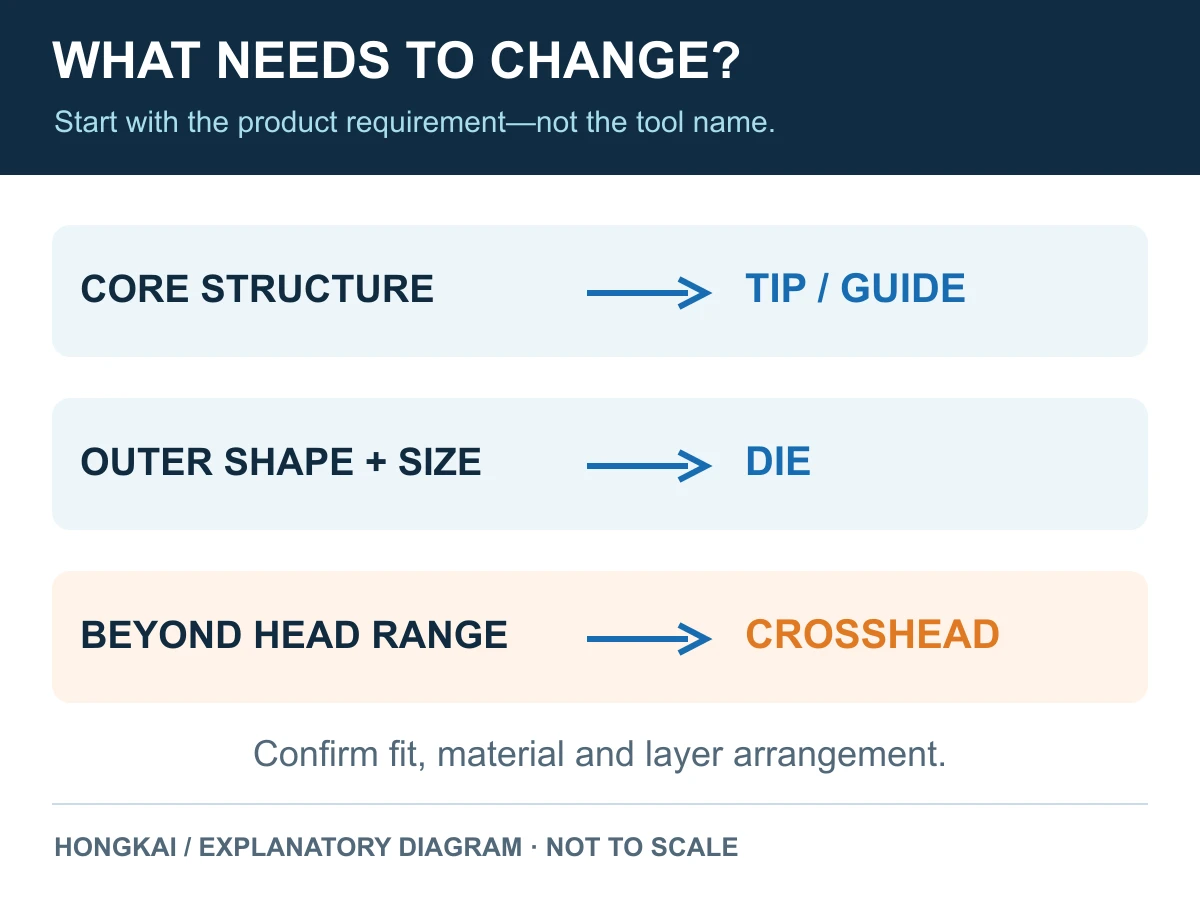
Explanatory decision map based on the application distinctions discussed for this guide. It is not a tooling drawing; fit, material and layer arrangement still require confirmation.
HONGKAI’s sizing discussions include U7, U10, U14 and U20 crossheads. In this family, the number indicates the supported maximum line-size range. Confirm the actual limit and which product dimension it refers to against the particular head’s drawing or specification. These names are not a universal sizing system across manufacturers.
For tooling, separate the incoming construction from the finished shape. A single-core and a two-core product can require different tips. The die must suit the target outer shape and size as well as the agreed material and extrusion method. Do not assume that each product change requires both tools to be replaced, or that a larger die can extend the head beyond its approved range.
| What changes? | ആദ്യം എന്ത് സമീക്ഷിക്കണം | എന്താണ് സ്ഥിരീകരിക്കേണ്ടത്? |
|---|---|---|
| ഏക-കോറിൽ നിന്ന് ദ്വി-കോറിലേക്ക് പോലുള്ള ഇൻകമിംഗ് കോർ നിർമ്മാണം | ടിപ്പ് അല്ലെങ്കിൽ ഗൈഡ് ജ്യാമിതി | പാസേജ്, മാർഗ്ഗനിർദ്ദേശ ഏർപ്പാട്, ഡൈയുമായുള്ള അനുയോജ്യത |
| ആവശ്യമായ പുറം ആകൃതി അല്ലെങ്കിൽ പൂർത്തിയാക്കിയ അളവ് | ഡൈ ജ്യാമിതിയും ഉപയോഗിക്കാവുന്ന പരിധിയും | തിരഞ്ഞെടുത്ത മെറ്റീരിയലും എക്സ്ട്രൂഷൻ രീതിയും ഉപയോഗിച്ച് ലക്ഷ്യമിട്ട ആകൃതിയും വലുപ്പവും |
| ആവശ്യമായ ഉൽപ്പന്ന വലിപ്പം ഹെഡിന്റെ സ്ഥിരീകരിച്ച പരിധിയെ അതിലംഘിക്കുന്നു | അനുയോജ്യമായ പരിധിയുള്ള ഒരു ഹെഡ് | പുതിയ ഹെഡ്, ടൂളിംഗ്, ലൈൻ ഇന്റർഫേസുകൾ എന്നിവ ഒരു പൂർണ്ണ പാക്കേജായി |
| പാളി ക്രമീകരണം, സ്ട്രൈപ്പ് അല്ലെങ്കിൽ മെറ്റീരിയൽ മാറ്റങ്ങൾ | എക്സ്ട്രൂഷൻ ഏർപ്പാട്, ഉപകരണത്തിന്റെ തുറന്ന ഭാഗം മാത്രമല്ല | ആവശ്യമായ ഫീഡുകൾ, അനുയോജ്യമായ ഹെഡ്/ടൂളിംഗ്, കൂടാതെ ഏതെങ്കിലും അപ്ലിക്കേഷൻ ട്രയൽ |
For an existing machine, provide its head identification, photographs and tooling drawing. Confirm the mounting dimensions, locating surfaces, holders and adjustment arrangement. Different manufacturers’ tools are not interchangeable merely because the finished cable diameter is the same.
HONGKAI’s published എക്സ്ട്രൂഷൻ സ്പെയർ-പാർട്ട്സ് പേജ് lists die, tip and adjusting-ring components and asks for photos or drawings before confirming a replacement. That is a starting point for part identification, not evidence that an unknown tool will fit every crosshead.
A worn part can help identify the assembly, but its measured dimensions should not automatically become the dimensions of a new part. Ask the supplier to distinguish the original design from wear, damage or earlier modifications. Record drawing revisions and part numbers so a later order refers to the same approved package.
Have the supplier record the agreed scope: replacement tools, a modified tooling package or a different head. That written boundary is more useful than an unsupported claim that one head can make every future product.
ഹെഡിനെ കുറ്റപ്പെടുത്തുന്നതിന് മുമ്പ് വയർ പാത പരിശോധിക്കുക
An uneven wall is a reason to investigate, not an automatic instruction to replace the crosshead. Preserve the sample and operating record before changing the setup. Record whether the issue appeared after a tool change, a material change, a restart or a change in line operation.
ഉൽപ്പാദനത്തിന് മുമ്പ് സെന്ററിംഗ് ഏർപ്പാട് സ്ഥാപിക്കുക
Identify whether the particular head uses manual adjustment, assisted adjustment or a fixed/self-centering arrangement. Follow the setup method for that design before formal production. A head described as requiring no routine centering adjustment still needs correct installation, matched tooling and a check of the finished wall.
ഇൻസ്റ്റാളേഷനും ട്രാക്ഷനും ഹെഡും പരിശോധിക്കുക
HONGKAI’s commissioning checks for the applications discussed here include equipment leveling, alignment between the crosshead’s cable path and the haul-off centerline, and abnormal haul-off vibration or jerking. Establish these conditions during installation rather than trying to compensate for them with the head’s centering adjustment later.
An uneven floor matters if the equipment has not been correctly supported and leveled. The floor does not have to serve as the alignment reference by itself. Ask the installer to verify the machine positions and cable path against the approved layout. A misaligned haul-off or unstable pull is a separate issue to correct; adjusting the head alone does not resolve it.

ലളിതമാക്കിയ അലൈൻമെന്റ് ആശയം, ഇൻസ്റ്റാളേഷൻ ഡ്രോയിംഗോ പൂർണ്ണമായ ഉൽപ്പാദന ലൈനോ അല്ല. ഉപകരണങ്ങളുടെ സ്ഥാനങ്ങളും, സപ്പോർട്ടുകളും, ടോളറൻസുകളും യഥാർത്ഥ ലേഔട്ട് പാലിക്കണം.
ഈ അന്വേഷണ ചോദ്യങ്ങൾ വേർതിരിച്ച് സൂക്ഷിക്കുക:
- Part identity: ഇൻസ്റ്റാൾ ചെയ്ത ടിപ്പ്, ഡൈ, ഹോൾഡറുകൾ എന്നിവ അംഗീകൃതമായ കോമ്പിനേഷനാണോ?
- Assembly condition: പരിശോധനയിൽ നാശം, മലിനീകരണം അല്ലെങ്കിൽ തിരുത്തൽ ആവശ്യമായ മറ്റേതെങ്കിലും അവസ്ഥ കാണിക്കുന്നുണ്ടോ?
- Line behavior: കോർ ഉദ്ദേശിച്ച പാതയിലൂടെ തുടർച്ചയായി പ്രവർത്തിക്കുന്നുണ്ടോ, അതോ അതിന്റെ സ്ഥാനമോ ടെൻഷനോ മാറുന്നുണ്ടോ?
- Heating behavior: തലയുടെ അളന്ന താപനിലകളും നിയന്ത്രണ പെരുമാറ്റവും അംഗീകൃത റെസിപ്പിനനുസരിച്ച് പൊരുത്തപ്പെടുന്നുണ്ടോ, അല്ലെങ്കിൽ ലക്ഷ്യിച്ച സെറ്റ്പോയിന്റുകൾ മാത്രം പ്രദർശിപ്പിക്കുന്നുണ്ടോ?
- Extrusion behavior: അംഗീകരിച്ച റെസിപ്പിയിൽ മെറ്റീരിയൽ തയ്യാറാക്കലും ഔട്ട്പുട്ടും സ്ഥിരതയുള്ളതാണോ?
- Measurement: റിപ്പോർട്ട് ചെയ്ത തകരാറ് ബാഹ്യ വ്യാസത്തിലുള്ള മാറ്റമോ, അസമമായ ചുമരിന്റെ കനം, അണ്ഡാകൃതിയോ അല്ലെങ്കിൽ ഇവയുടെ സംയോജനമോ ആണോ?
ഈ ചോദ്യങ്ങൾ തെളിവുകൾ ക്രമീകരിക്കുന്നു; ഒന്നും തനിയെ കാരണം സ്ഥാപിക്കുന്നില്ല. The വസ്തുവിന്റെയും പ്രക്രിയയുടെയും കുറവുകൾ അന്വേഷിക്കുന്നതിനുള്ള മാർഗ്ഗനിർദ്ദേശം ബുദ്ബുദങ്ങൾ, മൊരട്ടം അല്ലെങ്കിൽ അസ്ഥിരമായ എക്സ്ട്രൂഷൻ പ്രത്യക്ഷപ്പെടുമ്പോഴും അളവുപരമായ പ്രശ്നങ്ങൾക്കും വ്യാപകമായ പരിശോധനകൾ ഉൾക്കൊള്ളുന്നു.
If several settings are changed together, record all of them. A better sample after multiple changes cannot show which change solved the problem. Where a controlled comparison is practical, agree on the change and its evaluation before running the trial.
Note: Intrusive inspection, cleaning and tool changes require qualified personnel following the machine’s isolation, pressure-release and temperature-control instructions. This article does not authorize adjusting, opening or reaching into running or pressurized equipment.
ചുമരിന്റെ കനം അളക്കുക, പുറം വ്യാസം മാത്രമല്ല
A stable outside diameter does not prove that the conductor or core is centered. Accept the layer using the wall-thickness and dimensional evidence required by the cable specification, not only the diameter display.
SIKORA explains that comparing diameters before and after extrusion can provide a thickness value, but that laser-diameter comparison alone does not measure eccentricity. A system intended to measure eccentricity needs the relevant additional measurement capability.2
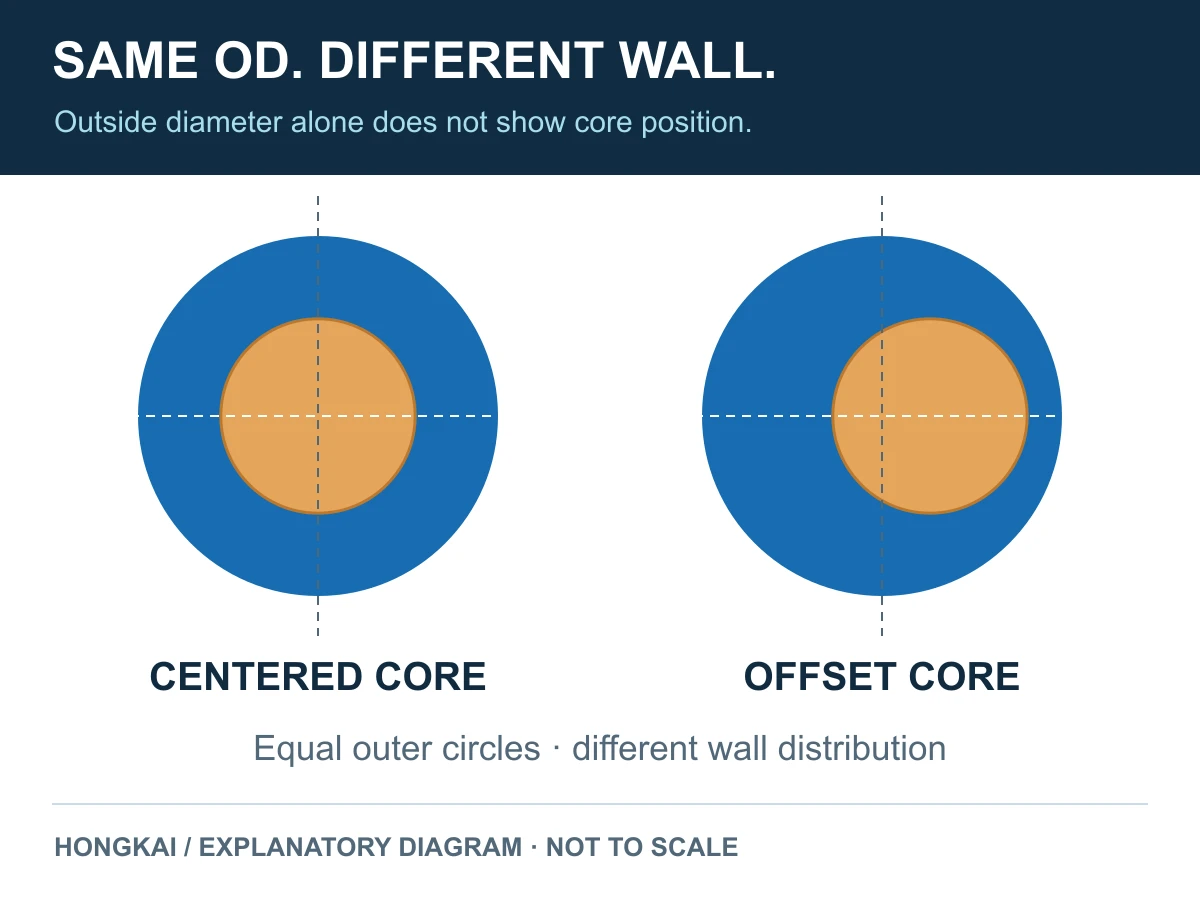
ഒരേ പുറം വ്യാസമുള്ള ആശയപരമായ ക്രോസ്-സെക്ഷനുകൾ. ഓഫ്സെറ്റ് കോർ ചുമരിന്റെ വിതരണത്തെ മാറ്റുന്നു; ഇവ അളന്ന സാമ്പിളുകളോ സ്വീകാര്യതാ പരിധികളോ അല്ല.
വാങ്ങലും പരീക്ഷണ രേഖകളും പരിശോധനാ നിബന്ധനകൾ വ്യക്തമായി സൂക്ഷിക്കുക:
| തെളിവ് | അത് സ്ഥാപിക്കാൻ സഹായിക്കുന്നത് എന്താണ് | അത് തനിയെ സ്ഥാപിക്കാത്തത് എന്താണ് |
|---|---|---|
| പുറം വ്യാസ രേഖ | അളക്കപ്പെട്ട ബാഹ്യ അളവിലുള്ള വ്യതിയാനം | പാളിയ്ക്കുള്ളിലെ കണ്ടക്ടറിന്റെയോ കോറിന്റെയോ സ്ഥാനം |
| തയ്യാറാക്കിയ ക്രോസ്-സെക്ഷൻ | ആ പ്രത്യേക സാമ്പിളിലെ ലോക്കൽ വാൾ ഡിസ്ട്രിബ്യൂഷൻ | മുഴുവൻ ഉൽപ്പാദന നീളത്തിന്റെയും നിലവാരം |
| യോജിച്ച ഓൺലൈൻ വാൾ അല്ലെങ്കിൽ എക്സെൻട്രിസിറ്റി മാപ്പിംഗ് | രേഖപ്പെടുത്തിയ റൺ സമയത്ത് അളക്കപ്പെട്ട പാരാമീറ്ററിന്റെ പെരുമാറ്റം | സ്ഥിരീകരിക്കാത്ത മെറ്റീരിയലിന്, വലിപ്പത്തിന് അല്ലെങ്കിൽ നിർമ്മാണ രീതിക്ക് യോജിച്ചത് |
| Surface inspection | പരിശോധന നടത്തിയ സ്ഥലത്തെ ദൃശ്യമായ രൂപം | എല്ലാ മറഞ്ഞിരിക്കുന്ന അളവുപരമായ അല്ലെങ്കിൽ വൈദ്യുത ആവശ്യങ്ങളും |
Before the trial, agree on how samples will be prepared and measured. Identify the instrument, the recorded quantities and the acceptance limits. Where a percentage such as “concentricity” appears in a proposal, require its definition and calculation method; do not assume that different reports use identical terminology.
Link each result to the same material batch, tooling setup and sample position or production time. If an online gauge and an offline sample disagree, first confirm that they refer to the same product and measurement conditions. Do not choose whichever result happens to be more favorable.
The measuring system also needs an application check. Ask which materials, layer arrangements, product dimensions and operating conditions it can evaluate in the proposed setup. This guide does not require a particular instrument brand or claim that one sensing method covers every cable.
ഒരു നല്ല സാമ്പിളിന് പകരം ആവർത്തിക്കാവുന്ന സെറ്റപ്പ് സ്വീകരിക്കുക
Agree on the trial before accepting the proposed crosshead or tooling change. Define the sample product, material grade, setup identity, operating conditions, measurement method and decision limits. The buyer and supplier should know what evidence will settle acceptance before the machine is demonstrated.
For the head itself, HONGKAI’s priorities in the applications discussed here are the actual product’s centering and normal heating behavior. Demonstrate both on the agreed product: inspect the wall distribution and retain the corresponding temperature records. These head-focused checks do not replace the other tests required for the finished cable.
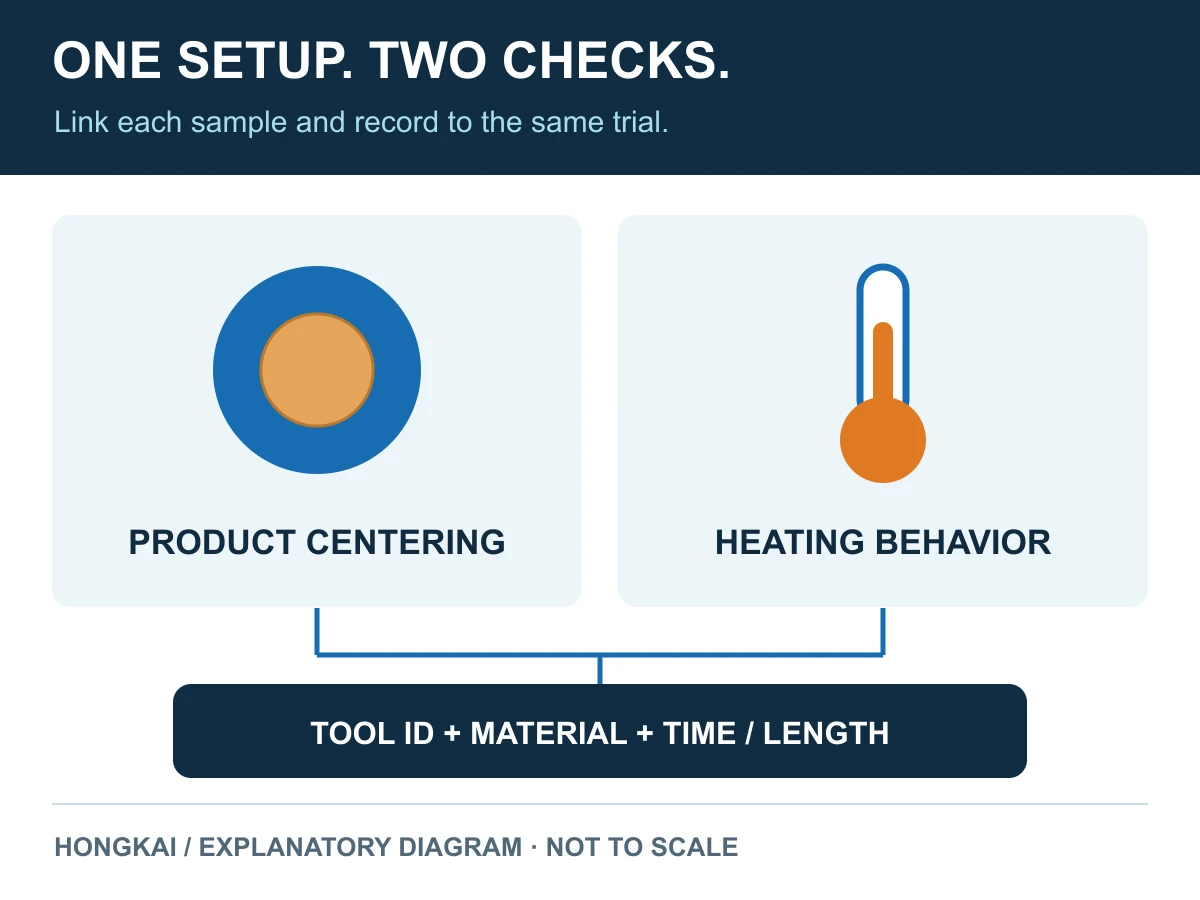
വിശദീകരണാത്മക രേഖാചിത്രം, പരീക്ഷണ റിപ്പോർട്ടല്ല. ലിങ്ക് സെന്ററിംഗ് സാമ്പിളുകളും താപനിലാ രേഖകളും ഒരേ സെറ്റപ്പുമായി ബന്ധിപ്പിക്കുക; യഥാർത്ഥ പരിധികളും മറ്റ് ഉൽപ്പന്ന പരീക്ഷണങ്ങളും പ്രത്യേകമായി ഉടമ്പടിക്കുക.
ഒരു ഉപയോഗപ്രദമായ പരീക്ഷണ റിക്കോർഡ് ഇനിപ്പറയുന്ന ഇനങ്ങളെ ബന്ധിപ്പിക്കുന്നു, അവയെ പരസ്പരബന്ധമില്ലാത്ത ഫോട്ടോകളായി സൂക്ഷിക്കുന്നതിന് പകരം:
- അംഗീകൃതമായ കേബിൾ ഡ്രോയിംഗും ഉപയോഗിച്ച കോമ്പൗണ്ട് ബാച്ചും.
- തല തിരിച്ചറിവ്, ഉപകരണ ഭാഗ നമ്പറുകൾ, ഡ്രോയിംഗ് റിവിഷനുകൾ.
- സെന്ററിംഗ് ഏർപ്പാട്, സ്ഥിരീകരിച്ച ലൈൻ അലൈൻമെന്റ്, കരാറായ ഓപ്പറേറ്റിംഗ് സാഹചര്യങ്ങൾ.
- നിർദ്ദിഷ്ട താപനിലാ ക്രമീകരണങ്ങളും അതിനനുസൃതമായ അളക്കപ്പെട്ട താപനിലാ രേഖകളും.
- സമയം അല്ലെങ്കിൽ നീള സൂചികളോടുകൂടിയ സൂക്ഷിച്ചിരിക്കുന്ന സാമ്പിളുകൾ.
- അനുബന്ധ അളവുപരമായ ഫലങ്ങളും മറ്റ് ബാധകമായ ഉൽപ്പന്ന പരിശോധനകളും.
- ഏതെങ്കിലും മുടക്കമോ ക്രമീകരണമോ, അതിന്റെ കാരണവും പിന്നീടുള്ള ഫലവും.
Where frequent product changes are important, include an agreed changeover in the demonstration. The question is not merely whether an experienced operator can produce one acceptable short sample. It is whether the factory can identify the approved tools, follow the documented setup and verify the result again under the agreed conditions.
Do not invent a universal test speed, duration or sample count. Those values must match the product, contract and factory’s acceptance method. Startup material and output made during an unapproved adjustment should remain identifiable under the factory’s quality procedure.
At handover, retain the accepted tool drawings or identifiers, setup instructions, maintenance guidance and sample records. List future materials and product sizes separately if they have not been demonstrated. A clear scope prevents the accepted setup for one cable from becoming an unsupported promise about every cable the factory may make later.
The strongest result is a matched tooling package with traceable samples and a repeatable setup. That gives production staff a basis for the next changeover and gives the buyer evidence for accepting the equipment.
-
ഗില്ലോ ടൂൾ & എഞ്ചിനീയറിംഗ്, സീരീസുകളും കോൺഫിഗറേഷൻ ഓപ്ഷനുകളും. Used only to substantiate the existence of distinct pressure/tubing and fixed/adjustable configurations, not as a HONGKAI product specification, supplier endorsement or universal selection rule. ↩
-
SIKORA, Thickness measurement, particularly the laser-measurement discussion. Supports the distinction between diameter-derived thickness and eccentricity measurement; no vendor-specific accuracy or performance claim is adopted. ↩