


A cable production manager may need new tooling after changing a cable size, adding a layer or finding uneven insulation. Before ordering a new crosshead, separate the cable requirement from the condition of the installed tooling and the way the line is running.
A new cable size does not always require a new crosshead. Check the incoming core structure, the required outside shape and size, and the head’s confirmed range. Then check line alignment, wall thickness and heating: changing tools or adjusting the head cannot correct every cause of an uneven wall.
This guide concerns the information and evidence needed for insulation and jacket extrusion. It is not a universal die-sizing recipe, a centering procedure for a particular machine or a substitute for its operating manual.
Начните со слоя, который наносится
Begin with a drawing of the product entering the crosshead and the product leaving it. A solid conductor, a stranded conductor and an assembled cable core should not be treated as interchangeable inputs simply because their nominal diameters are similar.
Record the incoming construction, its size range and the layer being applied. For a finished cable, identify whether the purchase concerns conductor insulation, an inner sheath or the outer jacket. Where several materials or layers are involved, identify them separately rather than requesting a generic “multilayer head.”
Подготовьте краткую карточку товара, содержащую:
- Чертеж входящего проводника или жилы и представительные образцы.
- Производитель компаунда, точная марка и рекомендации по переработке.
- Готовый наружный размер, требуемая толщина стенки и применимые пределы приемки.
- Количество и порядок слоев, включая любую полосу или другую отдельную подачу материала.
- Соответствующие требования к зачистке, адгезии или расслоению оболочек, если они включены в спецификацию кабеля.
- Текущий экструдер, идентификатор крестовины, компоновка линии и предполагаемый рабочий диапазон.
Выберите метод экструзии и расположение слоев отдельно
Pressure tooling and tubing tooling describe different extrusion approaches. Single-layer and coextrusion describe the layer arrangement. These are separate decisions, not four competing names for the same choice. Tooling manufacturers offer different pressure/tubing, layer and centering configurations.1
Start with the product and required wall thickness when choosing the extrusion approach. In the HONGKAI applications discussed for this guide, the optical-fiber tube operation uses tubing tooling, while the sheath operation uses pressure tooling. These are application examples, not a rule that every optical cable tube or jacket uses the same method.
Next, specify whether the product needs one layer, two layers in separate operations, or two layers extruded together. If both layers must be applied in one pass, the proposed head and material feeds must support that coextrusion arrangement. Identify a color stripe separately; a stripe is not automatically another complete sheath layer.
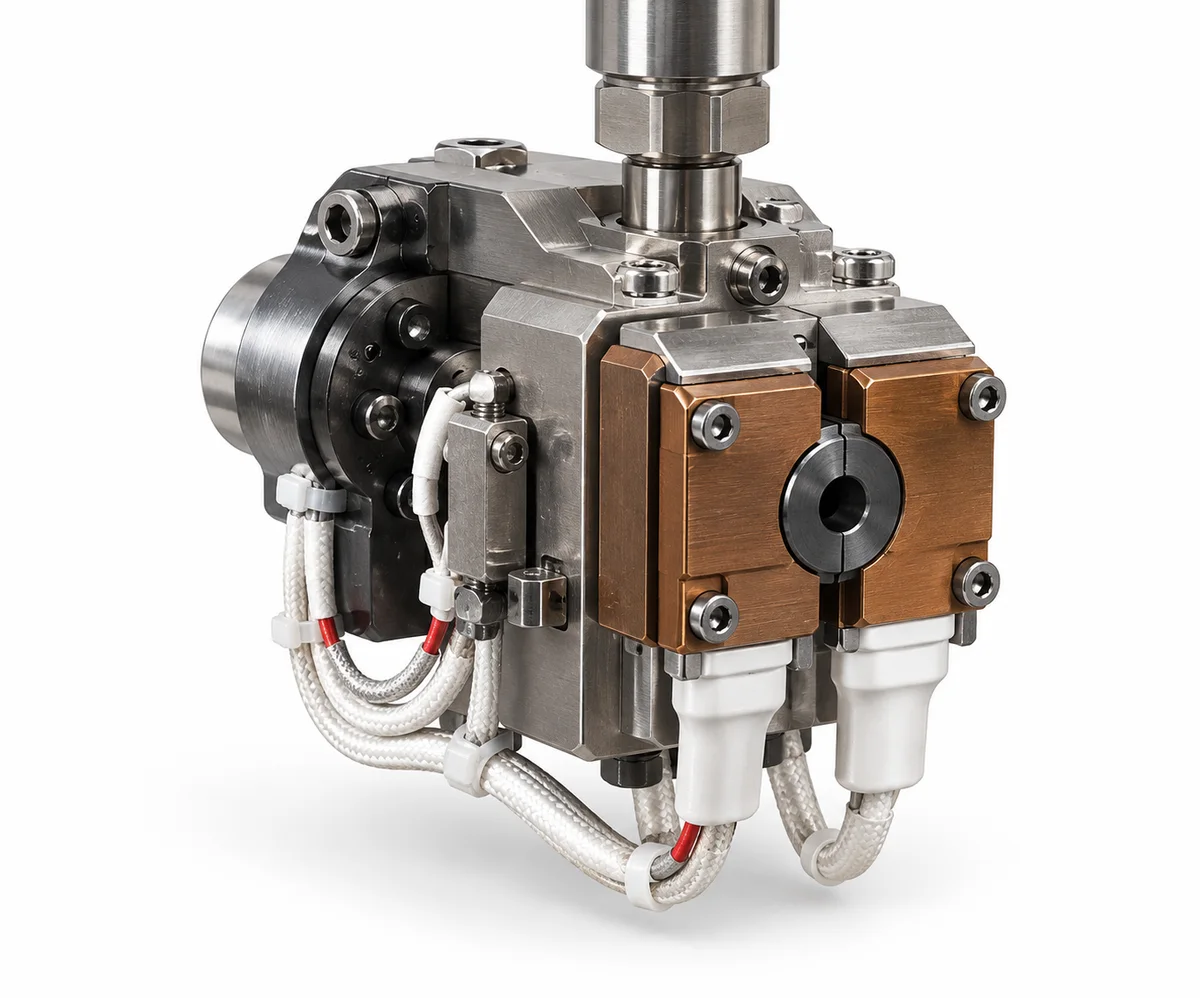
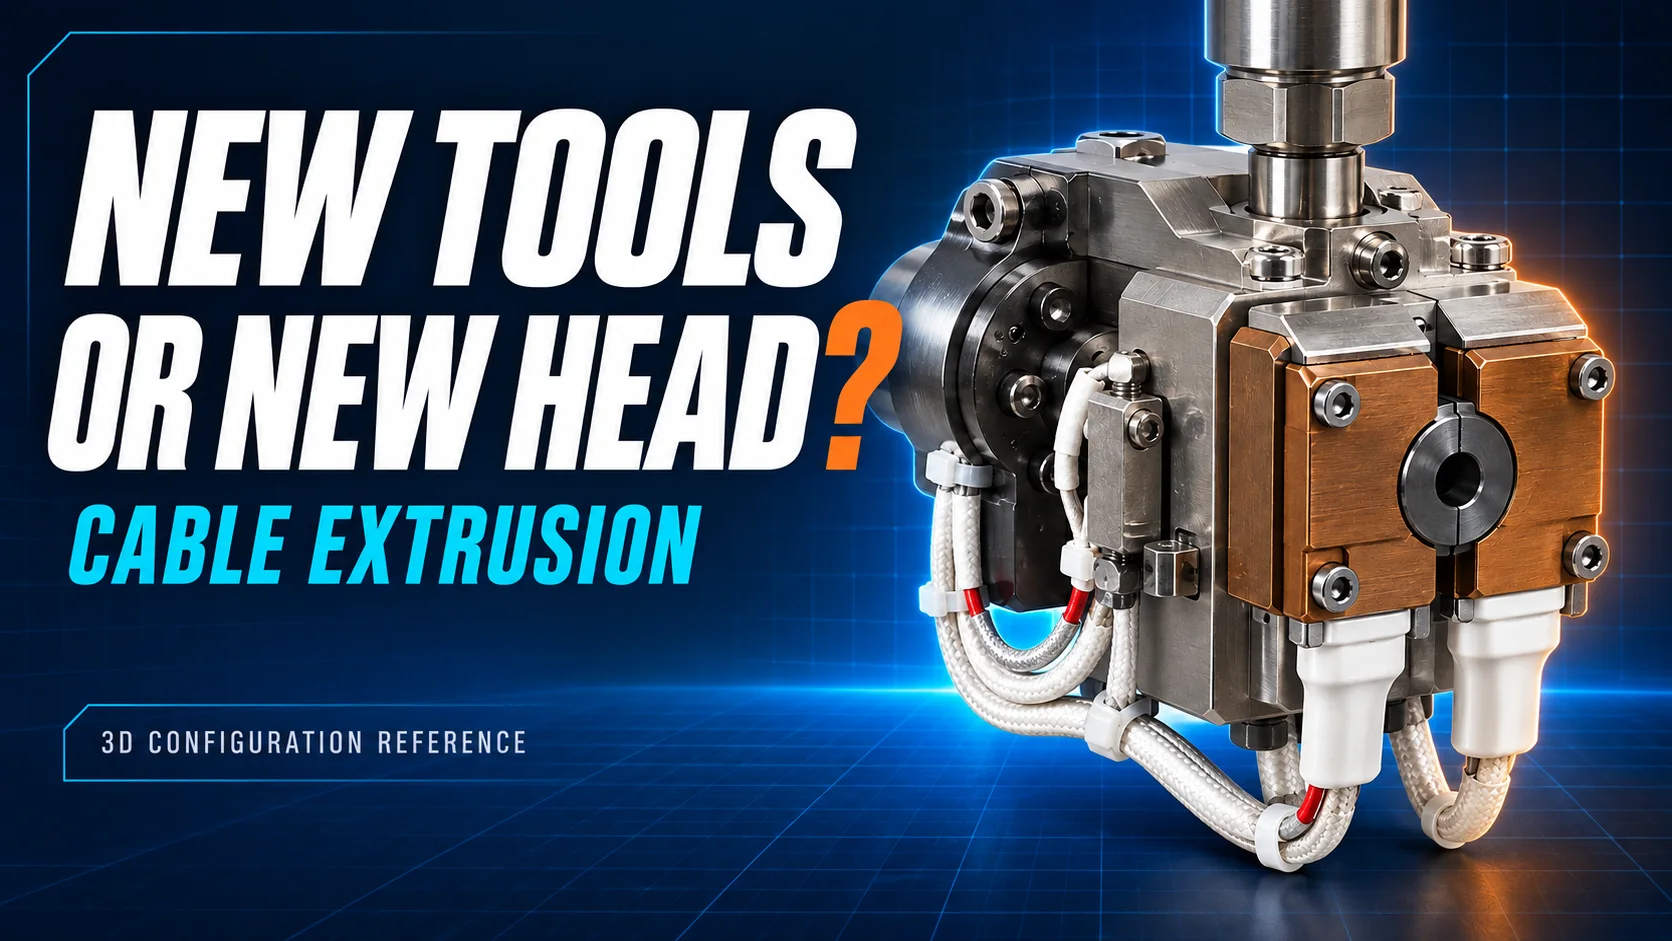
HONGKAI 3D exterior reference for a dual-layer coextrusion crosshead with a color-stripe arrangement. This is not a dimensioned drawing or a universal design for other crossheads.
For an expansion project, separate the first approved product from future products. Ask the supplier to identify which changes remain within the proposed head and tooling range, and which require a different setup or an application trial. A possible future configuration should not be listed as proven production scope.
Заменить инструменты или всю головку целиком?
Check the tip when the incoming core construction changes, and the die when the required outside shape or dimension changes. If the product is outside the installed head’s confirmed size range, a tooling change alone is not enough: the head must also change. Staying within that range is only the first compatibility check.
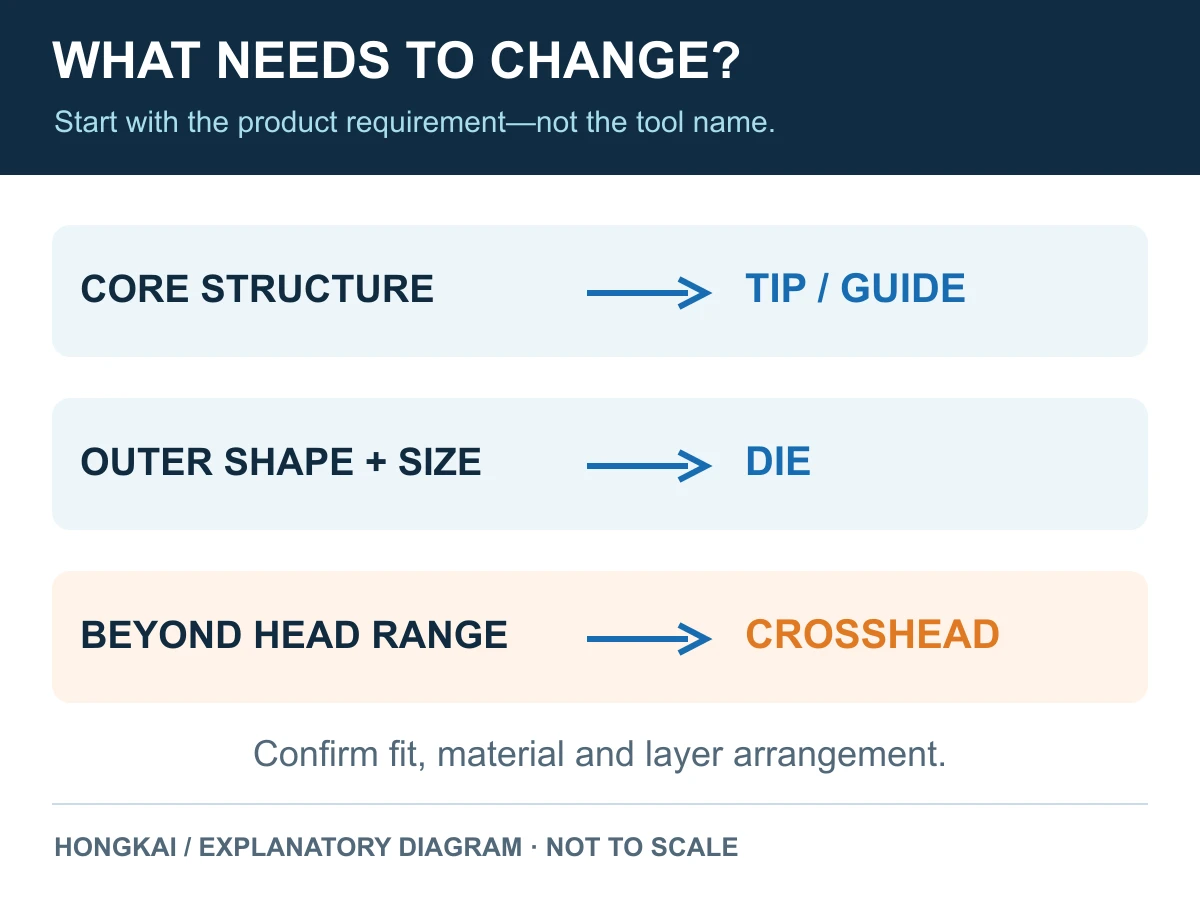
Explanatory decision map based on the application distinctions discussed for this guide. It is not a tooling drawing; fit, material and layer arrangement still require confirmation.
HONGKAI’s sizing discussions include U7, U10, U14 and U20 crossheads. In this family, the number indicates the supported maximum line-size range. Confirm the actual limit and which product dimension it refers to against the particular head’s drawing or specification. These names are not a universal sizing system across manufacturers.
For tooling, separate the incoming construction from the finished shape. A single-core and a two-core product can require different tips. The die must suit the target outer shape and size as well as the agreed material and extrusion method. Do not assume that each product change requires both tools to be replaced, or that a larger die can extend the head beyond its approved range.
| What changes? | Что проверить в первую очередь | Что необходимо подтвердить? |
|---|---|---|
| Входящая конструкция жилы, например, от одножильной до двухжильной | Геометрия наконечника или направляющей | Проход, направляющее устройство и совместимость с матрицей |
| Требуемая наружная форма или готовый размер | Геометрия матрицы и рабочий диапазон | Целевая форма и размер с выбранным материалом и методом экструзии |
| Требуемый размер изделия превышает подтвержденный предел головки | Головка с подходящим диапазоном | Новые головка, оснастка и интерфейсы линии в виде полного комплекта |
| Расположение слоев, изменение полосы или материала | Конфигурация экструзии, а не только отверстие инструмента | Требуемые подачи, совместимая головка/оснастка и любые испытания применения |
For an existing machine, provide its head identification, photographs and tooling drawing. Confirm the mounting dimensions, locating surfaces, holders and adjustment arrangement. Different manufacturers’ tools are not interchangeable merely because the finished cable diameter is the same.
HONGKAI’s published страница запасных частей для экструзии lists die, tip and adjusting-ring components and asks for photos or drawings before confirming a replacement. That is a starting point for part identification, not evidence that an unknown tool will fit every crosshead.
A worn part can help identify the assembly, but its measured dimensions should not automatically become the dimensions of a new part. Ask the supplier to distinguish the original design from wear, damage or earlier modifications. Record drawing revisions and part numbers so a later order refers to the same approved package.
Have the supplier record the agreed scope: replacement tools, a modified tooling package or a different head. That written boundary is more useful than an unsupported claim that one head can make every future product.
Проверьте путь провода перед тем, как винить головку
An uneven wall is a reason to investigate, not an automatic instruction to replace the crosshead. Preserve the sample and operating record before changing the setup. Record whether the issue appeared after a tool change, a material change, a restart or a change in line operation.
Установите центрирующее устройство перед началом производства
Identify whether the particular head uses manual adjustment, assisted adjustment or a fixed/self-centering arrangement. Follow the setup method for that design before formal production. A head described as requiring no routine centering adjustment still needs correct installation, matched tooling and a check of the finished wall.
Проверьте установку и тяговое усилие, а также головку
HONGKAI’s commissioning checks for the applications discussed here include equipment leveling, alignment between the crosshead’s cable path and the haul-off centerline, and abnormal haul-off vibration or jerking. Establish these conditions during installation rather than trying to compensate for them with the head’s centering adjustment later.
An uneven floor matters if the equipment has not been correctly supported and leveled. The floor does not have to serve as the alignment reference by itself. Ask the installer to verify the machine positions and cable path against the approved layout. A misaligned haul-off or unstable pull is a separate issue to correct; adjusting the head alone does not resolve it.

Упрощённая концепция выравнивания, не является монтажным чертежом или полной производственной линией. Расположение оборудования, опоры и допуски должны соответствовать фактической компоновке.
Сохраняйте эти вопросы для расследования отдельно:
- Part identity: Являются ли установленные наконечник, фильера и держатели утвержденной комбинацией?
- Assembly condition: Показывает ли осмотр повреждения, загрязнения или другое состояние, требующее исправления?
- Line behavior: Проходит ли сердечник равномерно по заданному пути или изменяются его положение или натяжение?
- Heating behavior: Соответствуют ли измеренные температуры головки и поведение системы управления утвержденному рецепту, а не только отображают заданные уставки?
- Extrusion behavior: Стабильны ли подготовка материала и выход продукции при утвержденном рецепте?
- Measurement: Является ли сообщенная неисправность изменением наружного диаметра, неравномерной толщиной стенки, овальностью или их комбинацией?
Эти вопросы систематизируют доказательства; ни один из них сам по себе не устанавливает причину. The руководство по расследованию дефектов материалов и технологических процессов охватывает более широкие проверки при появлении пузырей, шероховатости или нестабильной экструзии, а также при возникновении проблем с размерами.
If several settings are changed together, record all of them. A better sample after multiple changes cannot show which change solved the problem. Where a controlled comparison is practical, agree on the change and its evaluation before running the trial.
Note: Intrusive inspection, cleaning and tool changes require qualified personnel following the machine’s isolation, pressure-release and temperature-control instructions. This article does not authorize adjusting, opening or reaching into running or pressurized equipment.
Измеряйте толщину стенки, а не только наружный диаметр
A stable outside diameter does not prove that the conductor or core is centered. Accept the layer using the wall-thickness and dimensional evidence required by the cable specification, not only the diameter display.
SIKORA explains that comparing diameters before and after extrusion can provide a thickness value, but that laser-diameter comparison alone does not measure eccentricity. A system intended to measure eccentricity needs the relevant additional measurement capability.2
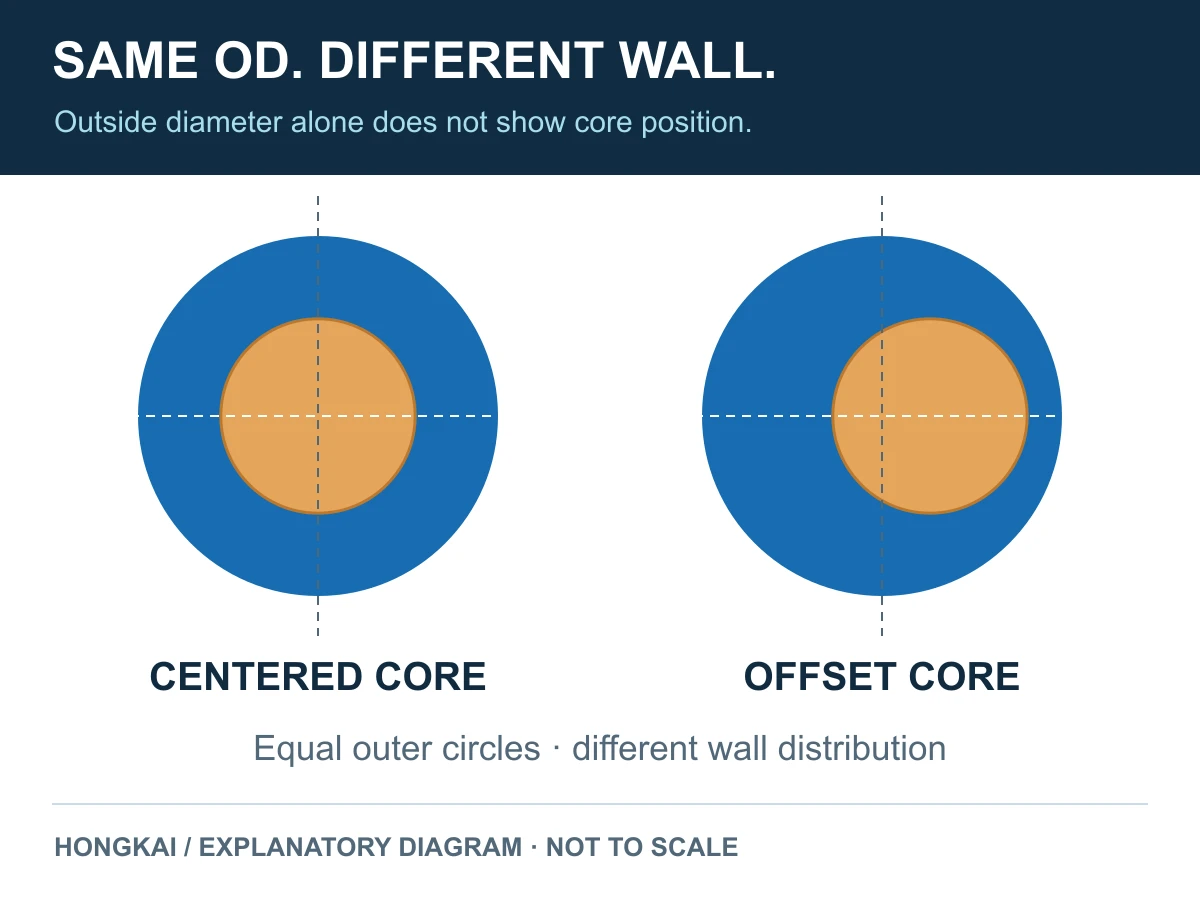
Концептуальные поперечные сечения с одинаковым наружным диаметром. Смещение сердечника изменяет распределение толщины стенки; данные не являются результатами измерений образцов или предельными значениями для приёмки.
Четко указывайте условия проверки в записях о покупке и испытаниях:
| Доказательства | Что это помогает установить | Что оно само по себе не устанавливает |
|---|---|---|
| Запись наружного диаметра | Вариация измеренного наружного размера | Положение проводника или жилы внутри слоя |
| Подготовленное поперечное сечение | Локальное распределение по стенке в данном конкретном образце | Качество всей длины продукции |
| Подходит для онлайн-измерения толщины стенки или эксцентриситета | Поведение измеряемого параметра во время зарегистрированного запуска | Пригодность для непроверенного материала, размера или конструкции |
| Surface inspection | Внешний вид в месте осмотра | Все скрытые размерные или электрические требования |
Before the trial, agree on how samples will be prepared and measured. Identify the instrument, the recorded quantities and the acceptance limits. Where a percentage such as “concentricity” appears in a proposal, require its definition and calculation method; do not assume that different reports use identical terminology.
Link each result to the same material batch, tooling setup and sample position or production time. If an online gauge and an offline sample disagree, first confirm that they refer to the same product and measurement conditions. Do not choose whichever result happens to be more favorable.
The measuring system also needs an application check. Ask which materials, layer arrangements, product dimensions and operating conditions it can evaluate in the proposed setup. This guide does not require a particular instrument brand or claim that one sensing method covers every cable.
Принимайте воспроизводимую настройку, а не один хороший образец
Agree on the trial before accepting the proposed crosshead or tooling change. Define the sample product, material grade, setup identity, operating conditions, measurement method and decision limits. The buyer and supplier should know what evidence will settle acceptance before the machine is demonstrated.
For the head itself, HONGKAI’s priorities in the applications discussed here are the actual product’s centering and normal heating behavior. Demonstrate both on the agreed product: inspect the wall distribution and retain the corresponding temperature records. These head-focused checks do not replace the other tests required for the finished cable.
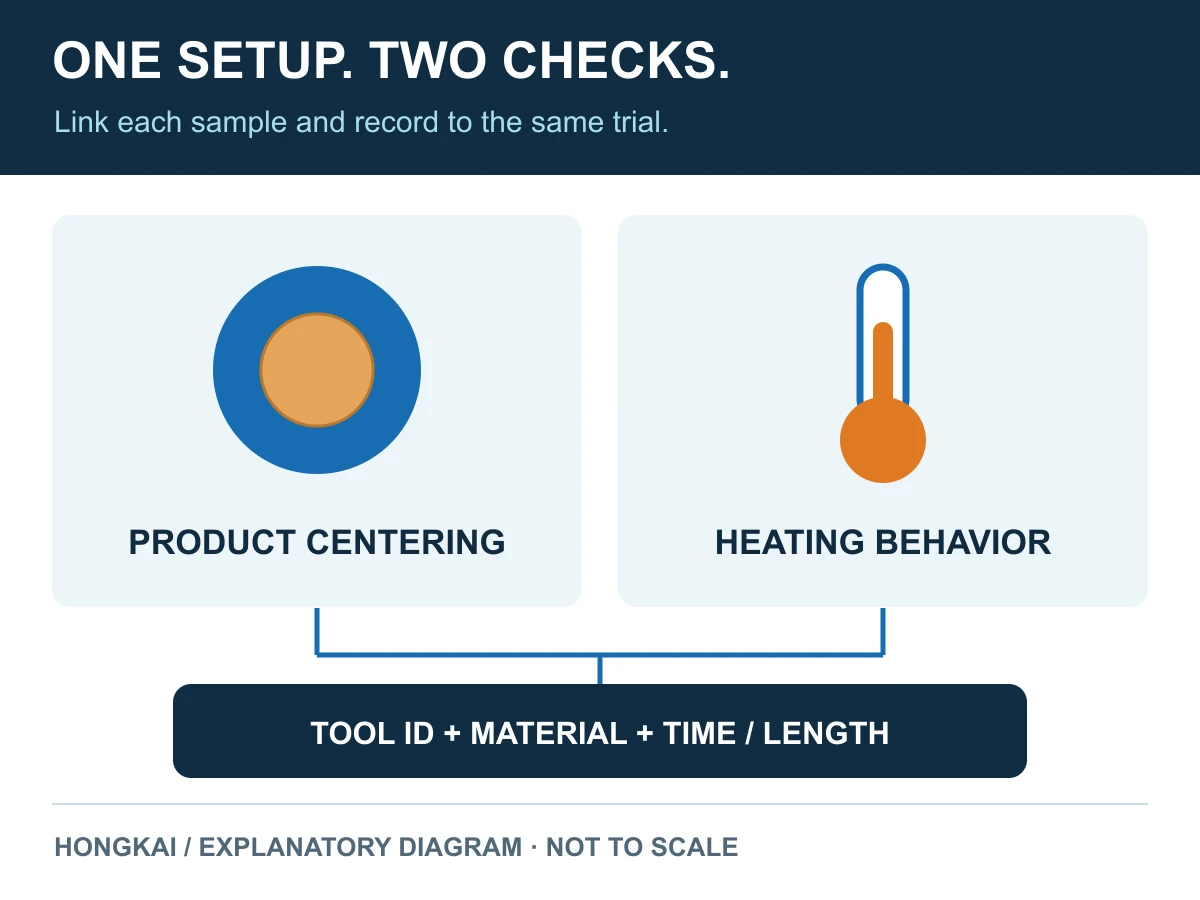
Пояснительная карта записи, а не отчет об испытаниях. Свяжите образцы центровки и температурные записи с одной и той же установкой; согласуйте фактические пределы и другие испытания продукции отдельно.
Полезная пробная запись связывает следующие элементы, а не сохраняет их как несвязанные фотографии:
- Утверждённый чертёж кабеля и использованная партия компаунда.
- Идентификация головки, номера инструментальных деталей и ревизии чертежей.
- Центрирующее устройство, проверенное выравнивание линии и согласованные условия эксплуатации.
- Указанные настройки температуры и соответствующие записи измеренных температур.
- Сохраненные образцы с указанием времени или длины.
- The corresponding dimensional results and other applicable product checks.
- Любое прерывание или регулировка, причина этого и последующий результат.
Where frequent product changes are important, include an agreed changeover in the demonstration. The question is not merely whether an experienced operator can produce one acceptable short sample. It is whether the factory can identify the approved tools, follow the documented setup and verify the result again under the agreed conditions.
Do not invent a universal test speed, duration or sample count. Those values must match the product, contract and factory’s acceptance method. Startup material and output made during an unapproved adjustment should remain identifiable under the factory’s quality procedure.
At handover, retain the accepted tool drawings or identifiers, setup instructions, maintenance guidance and sample records. List future materials and product sizes separately if they have not been demonstrated. A clear scope prevents the accepted setup for one cable from becoming an unsupported promise about every cable the factory may make later.
The strongest result is a matched tooling package with traceable samples and a repeatable setup. That gives production staff a basis for the next changeover and gives the buyer evidence for accepting the equipment.
-
Guill Tool & Engineering, Серии и варианты конфигурации. Used only to substantiate the existence of distinct pressure/tubing and fixed/adjustable configurations, not as a HONGKAI product specification, supplier endorsement or universal selection rule. ↩
-
SIKORA, Thickness measurement, particularly the laser-measurement discussion. Supports the distinction between diameter-derived thickness and eccentricity measurement; no vendor-specific accuracy or performance claim is adopted. ↩