


A wire bunching machine should be selected from the finished conductor backward, not from a reel size or maximum-speed headline. A factory owner or technical buyer must first define what enters the machine, what conductor must leave it, how that conductor will be tested, and which package must connect to the next process.
The correct wire bunching machine is the smallest project configuration that can produce the approved conductor across its required wire range, lay window and reel interface while maintaining controllable tension and measurable acceptance evidence. Nominal speed does not prove that the conductor will remain stable from an empty to a full take-up reel. The RFQ should therefore define the input wires, finished conductor, lay direction, packages, control functions, safeguards and FAT samples before a model is approved. HONGKAI can map those inputs to a machine family, but final performance must be confirmed against the exact cable and project conditions.
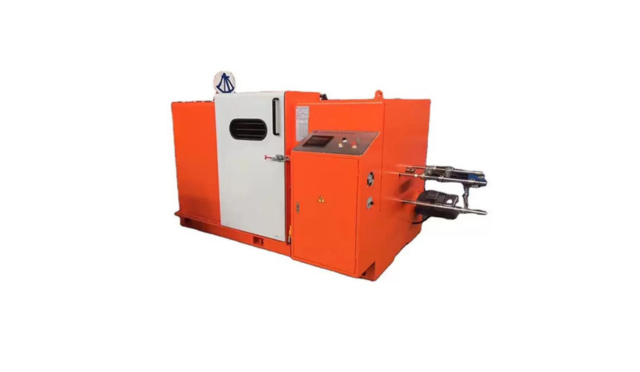
वास्तविक HONGKAI वायर बंचिंग मशीन संदर्भ। चयन चर्चा के लिए यह छोटा बंचर दिखाया गया है; सटीक मॉडल, इनपुट व्यवस्था और आपूर्ति की गई स्कोप को अभी भी प्रोजेक्ट विशिष्टता में पुष्टि किया जाना चाहिए।.
This guide is for low-voltage cable factory owners, production managers and technical procurement teams. It does not treat bunching, ordered stranding and cable laying-up as interchangeable names. The buyer’s decision is whether a proposed buncher matches one approved conductor design and whether the supplier can prove that match before shipment.
What Must Buyers Define Before Selecting a Wire Bunching Machine?
एक खरीदार को तार बंचिंग मशीन का चयन करने से पहले आठ जुड़े हुए निर्णयों को अंतिम रूप देना चाहिए: अंतिम चालक, इनपुट तार, लागू उत्पाद मानक, ले विंडो, रील इंटरफेस, तनाव विधि, सुरक्षा नियंत्रण और FAT प्रमाण। प्रत्येक निर्णय उपयोग योग्य मशीन कॉन्फ़िगरेशन और स्वीकृति पर आवश्यक प्रमाण को बदल देता है। स्क्रीनिंग के लिए एक विस्तृत कैटलॉग रेंज उपयोगी है, लेकिन यह अनुमोदित चालक ड्रॉइंग और नमूना योजना का स्थान नहीं ले सकती। आपूर्तिकर्ता को किसी मॉडल या स्थिर उत्पादन स्थिति की पुष्टि करने से पहले इनपुट-और-आउटपुट की पूर्ण परिभाषा की आवश्यकता होती है।.
1. Finished Conductor: Which conductor must the machine produce?
Why it matters: The finished conductor is the selection anchor. Nominal cross-sectional area alone does not state whether the conductor is bunched, concentrically stranded, compacted, flexible, coated, insulated or made to a special construction. Two conductors with the same nominal area can require different individual-wire counts, wire diameters, lay behavior, tension and downstream handling. A supplier cannot responsibly select a wire bunching machine from a cable name such as “flexible wire” without the approved construction.
What to ask: Send the finished-conductor drawing or specification with material, nominal area, construction class or product-standard reference, individual-wire count and diameter, finished diameter where controlled, coating or plating, direction, lay requirement, joint policy and downstream process. State whether the buncher receives bare wires, coated wires or already insulated cores. Mark every range as required, optional or future instead of combining unrelated products into one maximum envelope.
How to verify: Compare the supplier’s proposed operating window with every approved conductor at its smallest and largest required condition. Require the quotation to show which inputs were used to select the machine and which products remain outside the scope. IEC 60228:2023 covers nominal cross-sectional areas, wire numbers and sizes, and resistance values for several conductor types in power cables and cords, but the applicable finished-cable standard still decides whether IEC 60228 applies to the product.1
Red flags: The proposal lists only finished cable diameter, treats a conductor class as a machine model, assumes that all fine-wire conductors use the same process, or includes compacted and non-compacted constructions without separate tooling and acceptance review.
तय करें कि क्या एक बंचर, केज स्ट्रैंडर या कोई अन्य स्ट्रैंडिंग सिस्टम उपयुक्त है, इसके लिए व्यक्तिगत तार की सामग्री, व्यास और गिनती का उपयोग करें, साथ ही तैयार बाहरी व्यास, आवश्यक ले और तैयार उत्पाद की विशेषताओं का भी उपयोग करें। मार्ग नाममात्र चालक क्षेत्र या किसी सामान्य केबल नाम द्वारा निश्चित होने के बजाय उत्पाद-विशिष्ट रहता है।.
2. Input Wires: Are the material, diameter, count and condition complete?
Why it matters: A wire bunching machine handles individual inputs before it creates the finished bundle. Their material, diameter, count, surface, coating, hardness, incoming package and tension condition affect routing, guide contact, wire-break detection and the usable operating window. A machine that accepts the final nominal area on paper may still be unsuitable for the actual individual wires or packages.
What to ask: Define conductor material and coating, individual-wire diameter range, exact wire count for each product, incoming spool dimensions, flange and barrel condition, maximum approved package mass, payoff arrangement, allowable joints, surface cleanliness and any sensitivity to scratching or deformation. Identify whether the factory will buy prepared wire or draw, anneal or tin it on site. State the expected variation from upstream production rather than giving only a nominal value.
How to verify: Inspect the complete material path from every payoff position through guides and wire-break devices into the bunching zone. During FAT, use the agreed incoming packages and representative wires rather than substitute material chosen only because it runs easily. Confirm that guides, contact points and detection devices are suitable for the defined wire surface and that an input fault can be identified without damaging the retained conductor.
Red flags: The supplier selects a buncher from finished area only, the proposed payoff cannot accept the buyer’s actual spools, input wire count is described as “about” a value, or the FAT plan allows different wire material and package geometry from production.
जब चालक सामग्री, बंचन से पहले व्यक्तिगत तार का व्यास, तारों की संख्या, पूर्ण बाहरी व्यास या आवश्यक पूर्ण विशेषताएँ अनुपलब्ध हों, तो भले ही नाममात्र अनुप्रस्थ काट क्षेत्र पहले से ज्ञात हो, प्रस्ताव को प्रारंभिक मानें।.
3. Acceptance Basis: Which standard and finished tests control approval?
Why it matters: The wire bunching machine creates geometry, but the factory sells a conductor or cable that must meet an approved product specification. A visually uniform bundle does not prove conductor resistance, construction, dimensions or suitability for the next process. The buyer must separate machine functions from finished-product acceptance and name who supplies each test method and instrument.
What to ask: Identify the finished-cable standard, conductor clause, customer drawing and factory control plan that apply. State which properties are checked at the bunching stage and which are verified only after insulation or final cable production. Define sample conditioning, measurement temperature where relevant, instrument responsibility, pass/fail limits, record format and disposition of material made during setup or adjustment.
How to verify: Build an acceptance matrix that connects each requirement to a sample, test method, instrument, responsible party and retained record. If IEC 60228 applies, confirm the exact conductor type and edition rather than citing the standard as a general quality badge. The IEC publication record notes that its requirements generally relate to conductors in finished cable, so an intermediate bunching check must be connected to the finished-product control plan instead of being presented as automatic compliance.1
Red flags: The quotation says only “according to IEC,” a resistance result has no sample temperature or method, the FAT checks appearance but not the agreed conductor properties, or the supplier promises certification that neither the machine nor the FAT can establish.
4. Lay Window: Which lay length and direction must remain stable?
Why it matters: Lay length is a product setting, not a decorative parameter in a catalog table. The required window, S or Z direction, wire construction, speed and tension interact. A very wide nominal range is not useful if the machine cannot produce the buyer’s actual conductor with stable lay and acceptable handling under the agreed production condition.
What to ask: List every required lay length or approved range by conductor, the lay direction, tolerance and measurement method. Define whether settings change through gears, electronic control or another mechanism, and include the supplied change parts in the scope. Ask the supplier to state any speed, package or conductor condition that limits the requested lay window rather than quoting one universal maximum.
सत्यापित करने का तरीका: पहले अनुरोधित ले (lay) की तुलना सटीक प्रस्तावित मशीन के लिए पिच टेबल से करें। उस टेबल के भीतर एक मान केवल एक उम्मीदवार सेटिंग है, इसलिए मशीन के परीक्षण स्थिति तक पहुँचने के बाद सहमत FAT नमूनों पर वास्तविक ले मापें और जब परियोजना जोखिम इसे उचित ठहराता हो, तो एक से अधिक टेक-अप स्थिति में इसे दोहराएँ। रेसिपी या गियर संयोजन, दिशा, लाइन स्थिति, नमूना पहचान और परिणाम को रिकॉर्ड करें। HONGKAI की स्थानीय सामग्री में समीक्षित एक Φ800 कॉन्फ़िगरेशन इंटरचेंजेबल पिच गियर्स का उपयोग करता है और S या Z ऑपरेशन का समर्थन करता है; यह एक कॉन्फ़िगरेशन उदाहरण है, यह साबित नहीं करता कि प्रत्येक HONGKAI वायर बंचिंग मशीन एक ही तंत्र या सीमा का उपयोग करती है।.
Red flags: The supplier lists lay length without direction or tolerance, substitutes calculated pitch for measured conductor evidence, omits change gears or recipes from the supply, or promises the same stable speed at every lay and conductor condition.
अनुरोधित ले, जो सटीक मशीन टेबल के बाहर है, को स्कोप के बाहर रहना चाहिए जब तक कि संशोधित कॉन्फ़िगरेशन और नए उत्पाद प्रमाण सहमत न हो जाएँ। FAT के दौरान, अनुमोदित विधि का उपयोग करके ज्ञात नमूना लंबाई पर ले की गिनती या माप करके सेट मान की वास्तविक कंडक्टर से तुलना करें।.
5. Reel Interface: Do the payoff and take-up packages fit factory flow?
Why it matters: Reel diameter is only one interface. Flange condition, barrel diameter, traverse width, center hole, loading method, package mass, lifting access, traverse control and downstream handling decide whether the machine can be used safely and efficiently. A reel mismatch can delay commissioning even when the bunching head itself is suitable.
What to ask: Supply drawings or verified dimensions for every incoming and outgoing package, including tolerances and maximum approved mass. Define shafted or shaftless loading, lifting method, reel clamping, traverse range, loading aisle, finished package build and transfer to the next process. Confirm whether the supplied reel is a machine reel, shipping reel or production package and whether adapters are included.
How to verify: Load the agreed reels during FAT or perform a dimensional and functional interface check when production reels cannot be shipped. Run traverse across the usable width, inspect edge build and confirm that lifting, clamping, braking and removal can be completed by the approved method. Check the factory layout for actual reel movement and service access instead of assuming that machine footprint alone proves fit.
Red flags: A proposal says “800 mm reel” without a drawing, the flange fits but the center hole or traverse width does not, hydraulic lifting is listed without load and interface confirmation, or the buyer discovers after delivery that production reels cannot pass through the access route.
मशीन को अंतिम रूप देने से पहले प्रत्येक पेऑफ़ और टेक-अप स्थिति के आयामों की पुष्टि करें, चाहे व्यवस्था में एक रील हो या कई। कोई भी कस्टम पैकेज सप्लायर को इतनी पहले भेजें कि लोडिंग, क्लैंपिंग और ट्रैवर्स इंटरफ़ेस की जाँच या संशोधन किया जा सके। खाली से भरे तक तनाव जाँच के लिए, जब उपलब्ध हो तो मशीन डिस्प्ले रिकॉर्ड बरकरार रखें; अन्यथा दृश्य निर्णय पर भरोसा करने के बजाय एक नियंत्रित मैनुअल या यांत्रिक मापन विधि सहमत करें।.
6. Tension Control: How will the conductor remain stable from empty to full reel?
Why it matters: Take-up diameter changes during production, so the control system must manage tension as the package builds. Excess tension can deform or stretch fine wires; insufficient or unstable tension can disturb the bundle, traverse and downstream payoff. A named controller or magnetic-powder device is not evidence until the complete control behavior is demonstrated with the agreed conductor.
What to ask: Request the tension-control principle, sensing or feedback method, adjustment range, empty-to-full compensation, startup and slowdown behavior, recipe control, alarm conditions and operator permissions. Define how upstream payoff tension and downstream take-up tension are coordinated. Ask what evidence will show that adjustment can be made safely and that a wire break or abnormal condition does not leave uncontrolled stored motion.
How to verify: Observe startup, steady running, speed change, controlled stop and representative package build. Retain the operating settings and inspect the conductor, lay, reel build and any tension record available from the system. A local Φ800 reference configuration reviewed by HONGKAI uses PLC tracking with magnetic-powder take-up tension; the project still needs conductor-specific FAT evidence before that control concept can be accepted.
Red flags: The supplier describes tension as “automatic” without a control explanation, FAT starts with a partly filled reel only, operators can overwrite settings without control, or the machine remains running after an input-wire break.
7. Safety Controls: Which hazards and automatic stops must be verified?
Why it matters: High-speed rotating equipment, moving reels, stored tension and electrical systems create hazards that must be addressed by the machine design, factory risk assessment and operating controls. A closed cover or emergency-stop button alone does not prove that all hazards are controlled. The acceptance plan should verify the safeguards supplied with the exact configuration and the interfaces that remain the buyer’s responsibility.
What to ask: Require a machine-specific risk and safeguard review, guarding and interlock description, emergency-stop functions, wire-break and door-open behavior, braking method, safe reel-loading procedure, isolation points, warning labels and required factory utilities. Define the stopping and restart sequence after each protective event. State who supplies external fencing, lifting devices, compressed air, foundations and site electrical protection where applicable.
How to verify: Test agreed protective functions during FAT without bypassing safeguards. Confirm that the final electrical documentation matches the supplied machine and that faults require an intentional, controlled reset. IEC 60204-1:2016 with Amendment 1:2021 applies to electrical, electronic and programmable electronic equipment of machines from the supply connection, while ISO 12100:2010 provides risk-assessment and risk-reduction principles.23
Red flags: A safety door is shown but not interlocked, a stop test is skipped because it interrupts production, braking behavior is not defined, or the proposal uses a standard number as a certification claim without project-specific evidence.
8. FAT Evidence: Which sample and records prove the machine is acceptable?
Why it matters: A no-load rotation test proves assembly and basic control only. The buyer needs evidence that the wire bunching machine can handle representative inputs, produce the agreed lay and package, respond to faults and transfer usable conductor to the next stage. FAT should be designed before the order so the supplier can prepare material, reels, tooling and test instruments.
What to ask: Define the FAT conductor or conductor family, input wire, package state, lay, direction, run condition, sampling points, measured properties, safeguards to test, documents to review and treatment of open items. Include the expected recipe, tooling and change parts in the record. Separate witness tests from supplier pre-tests and state which raw results, photographs, videos and sample lengths the buyer receives.
How to verify: Trace one sample from identified input reels through the machine settings to the finished reel and retained test record. Compare the actual supplied machine, nameplates, drawings, software or recipe version, spares and tooling with the signed scope. Repeat a setting change or fault recovery when it is material to production, then confirm that the resulting conductor still meets the agreed acceptance basis.
Red flags: FAT uses unidentified material, the accepted conductor differs from the buyer’s smallest or most demanding product without written rationale, only a short edited video is retained, or deviations are closed verbally without owner, date and verification evidence.
निर्णय मानदंड: पुष्टि किए गए अंतिम बाहरी व्यास और अनुरोधित ले (lay) से FAT कंडक्टर चुनें, जिसमें वह ऑपरेटिंग स्थिति शामिल हो जो सहमत ले-और-गति संयोजन को सबसे अधिक मांग वाला बनाती है। ज्ञात लंबाई पर वास्तविक नमूने के खिलाफ मशीन सेटिंग की जांच करें। मेल खाता परिणाम केवल उस नमूने के लिए पिच स्थिति को प्रदर्शित करता है; यह किसी अपरीक्षित कंडक्टर या गति को सिद्ध नहीं करता।.
Note: A buncher is ready for selection only when its input, output, package, control and acceptance boundaries can all be written into the same project specification.
How Should a Buyer Compare Wire Bunching Machine Models?
Wire bunching machine models should be compared by required operating overlap, not by choosing the largest reel or fastest catalog value. The usable model must cover the individual wires, finished conductor, lay window and package interfaces at the same time. Controls, safeguards, change parts, access and downstream handling then decide whether that mechanical range is practical. HONGKAI’s current product family is a screening reference; the signed project specification must remain the final authority.
वर्तमान HONGKAI wire bunching machine page presents several model sizes from HK-300 through HK-1250. Its table changes input range, finished-conductor range, lay range, reel, rotational speed, drive and machine dimensions by model. Buyers should use that page to identify candidates, then require a returned selection matrix based on the actual conductor list.
| तुलना प्रश्न | खरीददार द्वारा प्रदान किए गए साक्ष्य | आपूर्तिकर्ता द्वारा लौटाए गए साक्ष्य |
|---|---|---|
| क्या मॉडल प्रत्येक आवश्यक व्यक्तिगत तार को स्वीकार करता है? | उत्पाद द्वारा सामग्री, परिपत्र, व्यास, गिनती और आगमन पैकेज | उपयोगयोग्य इनपुट विंडो और अनुपयुक्त स्थितियाँ |
| क्या मॉडल प्रत्येक अनुमोदित चालक बना सकता है? | निर्माण, समाप्त क्षेत्र, आयाम, ले और मानक | चयनित मॉडल, उपकरण और उत्पाद-द्वारा-उत्पाद मैपिंग |
| क्या आवश्यक ले व्यावहारिक है? | ले मान, दिशा, सहिष्णुता और माप विधि | सेटिंग विधि, बदले जाने वाले भाग और सीमा शर्तें |
| क्या पैकेज कारखाने से जुड़ते हैं? | पेऑफ और टेकअप ड्राइंग, द्रव्यमान और हैंडलिंग रूट | रील इंटरफेस, एडेप्टर, ट्रैवर्स और लोडिंग विधि |
| क्या नियंत्रण उत्पादन स्थिति को प्रबंधित कर सकते हैं? | उत्पाद मिश्रण, परिवर्तन और ऑपरेटर सीमाएँ | तनाव अवधारणा, रेसिपी, अलार्म और अनुमतियाँ |
| क्या दायरा स्वीकार्य है? | FAT नमूने, परीक्षण, उपकरण और रिकॉर्ड | प्री-टेस्ट योजना, साक्षी योजना और विचलन प्रक्रिया |
एक बड़ी मशीन स्वतः एक सुरक्षित निवेश नहीं होती। इससे फर्श का स्थान, घूर्णन द्रव्यमान, पैकेज हैंडलिंग, पहुँच, उपयोगिताएँ और छोटे उत्पादों की आर्थिकता बदल सकती है। एक छोटी मशीन स्वतः अधिक कुशल नहीं होती अगर यह एक योजनाबद्ध चालक को बाहर रखती है या दूसरी प्रक्रिया में अक्सर स्थानांतरण की आवश्यकता होती है। खरीददार को स्वीकृत वर्तमान श्रेणी और एक वास्तविक भविष्य की श्रेणी की तुलना करनी चाहिए, फिर हर अन्य संभावना को दायरे के बाहर लेबल करना चाहिए।.
A local Φ800 HONGKAI reference configuration includes a Siemens PLC, Weinview touchscreen, magnetic-powder take-up tension, electromagnetic braking, oil-pump reel lifting, wire-break and door-open stops, digital length measurement, interchangeable pitch gears and a defined spare-tool set. Those functions are useful RFQ prompts. They are not a universal HONGKAI specification, and every brand, range, power value, reel dimension and control function must be reissued for the selected project.
जब पुष्टि किए गए उत्पाद में बड़ी मशीन की व्यावहारिक सीमा से बाहर के बारीक तारों का उपयोग होता है, तो एक समर्पित छोटी मशीन का मूल्यांकन किया जाना चाहिए। केवल तभी एक व्यापक-सीमा वाली मशीन का औचित्य सिद्ध होता है जब कोई नामित भविष्य का कंडक्टर अपनी सामग्री, अलग-अलग तारों, पूर्ण व्यास, ले और रीलों को किसी सत्यापित मशीन विंडो से मैप करता हो। उस उत्पाद परिभाषा के बिना “भविष्य का विस्तार” अप्रयुक्त सीमा खरीदने का कारण नहीं है।.
अतः अंतिम तुलना में यह दिखाया जाना चाहिए कि खरीददार के उत्पाद कहाँ प्रस्तावित मॉडल के साथ ओवरलैप करते हैं और कहाँ नहीं करते। कोई भी दावा किया गया भविष्य क्षमता को एक नामित चालक, टूलिंग सेट, पैकेज और परीक्षण योजना से जोड़ा जाना चाहिए। उन विवरणों के बिना “विस्तारणीय” एक इंजीनियरिंग सीमा नहीं है।.
नोट: मॉडल आकार स्वीकृत चालक पोर्टफोलियो का परिणाम है, चयन प्रक्रिया में पहला निर्णय नहीं।.
एक तार बंडलिंग मशीन को स्वीकृति देने से पहले RFQ और FAT को क्या आवश्यकता होनी चाहिए?
एक पूर्ण RFQ आपूर्तिकर्ता को बिना अनुमान लगाए एक तार बंडलिंग मशीन चुनने की अनुमति देना चाहिए, और एक पूर्ण FAT योजना को स्वीकृति आधार को बदले बिना वापसी वाली कॉन्फ़िगरेशन को साबित करना चाहिए। खरीददार को उत्पाद, इनपुट-तार, रील, लेआउट, उपयोगिता, नियंत्रण और परीक्षण डेटा को एक नियंत्रित पैकेज में जोड़ना चाहिए। आपूर्तिकर्ता को एक मॉडल-चयन मैट्रिक्स, पूर्ण दायरा, अपवाद, ड्राइंग, नियंत्रण विवरण और नमूना योजना वापस करनी चाहिए। अनसुलझे तकनीकी अनुमानों को हस्ताक्षरित आवश्यकताओं में बदल दिए जाने या स्पष्ट रूप से अपवर्जित शर्तों में बदल दिए जाने तक स्वीकृति लंबित रहनी चाहिए।.
- ☐ स्वीकृत फिनिश्ड चालक ड्राइंग और लागू केबल मानक
- ☐ व्यक्तिगत तार सामग्री, कोटिंग, व्यास, गिनती और विचलन
- ☐ फिनिश्ड चालक क्षेत्र, निर्माण, आयाम और प्रतिरोध आधार
- ☐ आवश्यक ले लंबाई, सहिष्णुता, दिशा और मापन विधि
- ☐ आगमन और निर्गम रील ड्राइंग, पैकेज द्रव्यमान और लोडिंग विधि
- ☐ पेऑफ स्कोप, तनाव विधि, तार टूटने का पता लगाना और गाइड व्यवस्था
- ☐ लेने वाला तनाव अवधारणा, ट्रैवर्स, खाली से पूर्ण व्यवहार और रेसिपी
- ☐ आवश्यक बदले जा सकने वाले गियर, टूलिंग, एडाप्टर और आपूर्ति किए गए उत्पादन रील
- ☐ गार्डिंग, इंटरलॉक्स, आपातकालीन रोक, ब्रेकिंग और अलगाव जानकारी
- ☐ बिजली आपूर्ति, संपीड़ित वायु, फर्श लोडिंग, पहुँच और उठाने की सीमाएँ
- ☐ ऑपरेटर नियंत्रण स्तर, अलार्म, दोष इतिहास और बैकअप जिम्मेदारी
- ☐ FAT सामग्री, नमूना पहचान, चलने की स्थिति और साक्षी बिंदु
- ☐ एलएवाई, डीआईएमईएनएसआईओएनएस, आरईएसआईएसटीएएनसीई एएनडी डीओडब्ल्यूएनएसटीआरईएएम-एचएएनडीएलआईएनजी एएसीसीईपीटीएएनसीई ईवीआईडीईएनसीई
- ☐ Protective-function and controlled fault-recovery tests
- ☐ एमईसीएचएएनआईसीएएल, ईएलईसीटीआरआईसीएएल एएनडी यूटीआईएलआईटीवाई डीआरएडब्ल्यूआईएनजीएस एमएटीसीएचआईएनजी टीएचई दउप्पलीडएआईईड आरईवीआईएसआईओएन
- ☐ उपकरण, अतिरिक्त भाग, मैनुअल, नुस्खे और प्रशिक्षण कार्यक्षेत्र में शामिल हैं
- ☐ विचलन, बहिष्कार और उत्तरदायी मालिकों के साथ भविष्य के उत्पाद
जारी करने से पहले, खरीदार को विरोधाभासी रेंज हटा देनी चाहिए और वर्तमान उत्पादों को संभावित भविष्य के उत्पादों से अलग कर देना चाहिए। एक विशिष्टता को एक साथ सबसे छोटे फाइन-वायर उत्पाद, सबसे बड़े भविष्य के कंडक्टर और अधिकतम गति की मांग नहीं करनी चाहिए, जब तक कि परियोजना को वास्तव में उस संयोजन की आवश्यकता न हो और आपूर्तिकर्ता उसका परीक्षण कर सकता हो। यदि एक से अधिक मशीन परिवार तकनीकी रूप से उचित हैं, तो पैकेज, फर्श का क्षेत्रफल, चेंजओवर, स्थिर संचालन विंडो और प्रमाण में ट्रेड-ऑफ का अनुरोध करें, बजाय किसी एक अस्पष्ट अनुशंसा के लिए कहने के।.
FAT पर, पहचान से शुरुआत करें। मशीन मॉडल, आपूर्ति किए गए घटकों, ड्रॉइंग्स, सुरक्षा ढाल, नियंत्रण संस्करण, टूलिंग और रील्स को हस्ताक्षरित दायरे के विरुद्ध पुष्टि करें। फिर सहमत कंडक्टर को पहचाने गए इनपुट पैकेजों से लेकर सेटिंग्स और सुरक्षात्मक कार्यों के माध्यम से अंतिम रील तक ट्रेस करें। कच्चे मापन रिकॉर्ड और अनसुलझे मुद्दों को संरक्षित रखें, न कि केवल एक प्रचार वीडियो।.
अगले चरण का इंटरफ़ेस स्वीकृति का हिस्सा है। एक चालक, बंचिंग-चरण की उपस्थिति जांच में तो उत्तीर्ण हो सकता है, परंतु यदि रील बिल्ड, पेऑफ़ व्यवहार, सतह या तनाव इतिहास अनुपयुक्त है, तो एक्सट्रूज़न या केबलिंग के दौरान समस्या पैदा कर सकता है। जहां व्यावहारिक हो, डाउनस्ट्रीम सत्यापन के लिए पर्याप्त पहचाने गए चालक को बरकरार रखें या किसी अन्य परियोजना-विशिष्ट विधि पर सहमति बनाएं। अंतिम केबल रिलीज़ फिर भी स्वीकृत तैयार-उत्पाद नियंत्रण योजना के अनुसार होती है।.
यदि कारखाना एकल मशीन के बजाय एक पूर्ण कम वोल्टेज मार्ग की तुलना कर रहा है, तो HONGKAI का उपयोग करें कम वोल्टेज केबल उत्पादन लाइन चयन गाइड चालक तैयारी, बंडलिंग, इंसुलेशन, केबलिंग, शर्ती सुरक्षा, शीथिंग, परीक्षण और हैंडलिंग को मैप करने के लिए। जब अनुमोदित चालक निर्माण इसकी आवश्यकता करे, तभी तार बंडलिंग मशीन उस मार्ग पर प्रवेश करनी चाहिए।.
नोट: एक खरीद निर्णय तब ऑडिट करने योग्य होता है जब कोई अन्य इंजीनियर यह दोहरा सके कि मॉडल क्यों चुना गया, इसे क्या उत्पादित करना है, इसकी परीक्षा कैसे की जाएगी और कौन सी शर्तें परिधि के बाहर हैं।.
-
IEC 60228:2023, Conductors of insulated cables. आधिकारिक IEC रिकॉर्ड बिजली केबल और कोर्ड में कई प्रकार के चालकों के लिए नाममात्र अनुप्रस्थ काट क्षेत्रफल, तार संख्याएँ और आकार, और प्रतिरोध मानों को कवर करता है; लागू होना केबल मानक पर निर्भर करता है।↩ ↩
-
IEC 60204-1:2016, Safety of machinery — Electrical equipment of machines — Part 1, संशोधन 1 के साथ:2021 available IEC प्रकाशन रिकॉर्ड से उपलब्ध है। यह मशीनों के आपूर्ति संयोजन से विद्युत, इलेक्ट्रॉनिक और प्रोग्राम करने योग्य इलेक्ट्रॉनिक उपकरणों को कवर करता है।↩
-
ISO 12100:2010, Safety of machinery — General principles for design — Risk assessment and risk reduction. ISO बताता है कि मानक की अंतिम समीक्षा और पुष्टि 2022 में की गई थी, जबकि एक संशोधन विकासाधीन है।↩
 English
 हिन्दी
 فارسی