


A low-voltage cable factory owner should not start an equipment enquiry with a generic request for “one cable line.” Building wire, THHN or THWN, flexible cable and control cable can share some processes, but their conductor construction, applied layers, core assembly, testing and finished handling create different production routes.
The correct low-voltage cable production line starts with one approved finished-cable design, not a machine model. A buyer should define the conductor, insulation and covering layers, number of cores, protection elements, target package and acceptance basis before equipment is selected. Only the required stages should enter the project scope, and every interface between those stages should be written into the quotation and factory acceptance test. HONGKAI can then map the confirmed design to a project-specific combination of conductor preparation, bunching or stranding, extrusion, assembly, testing and handling equipment.
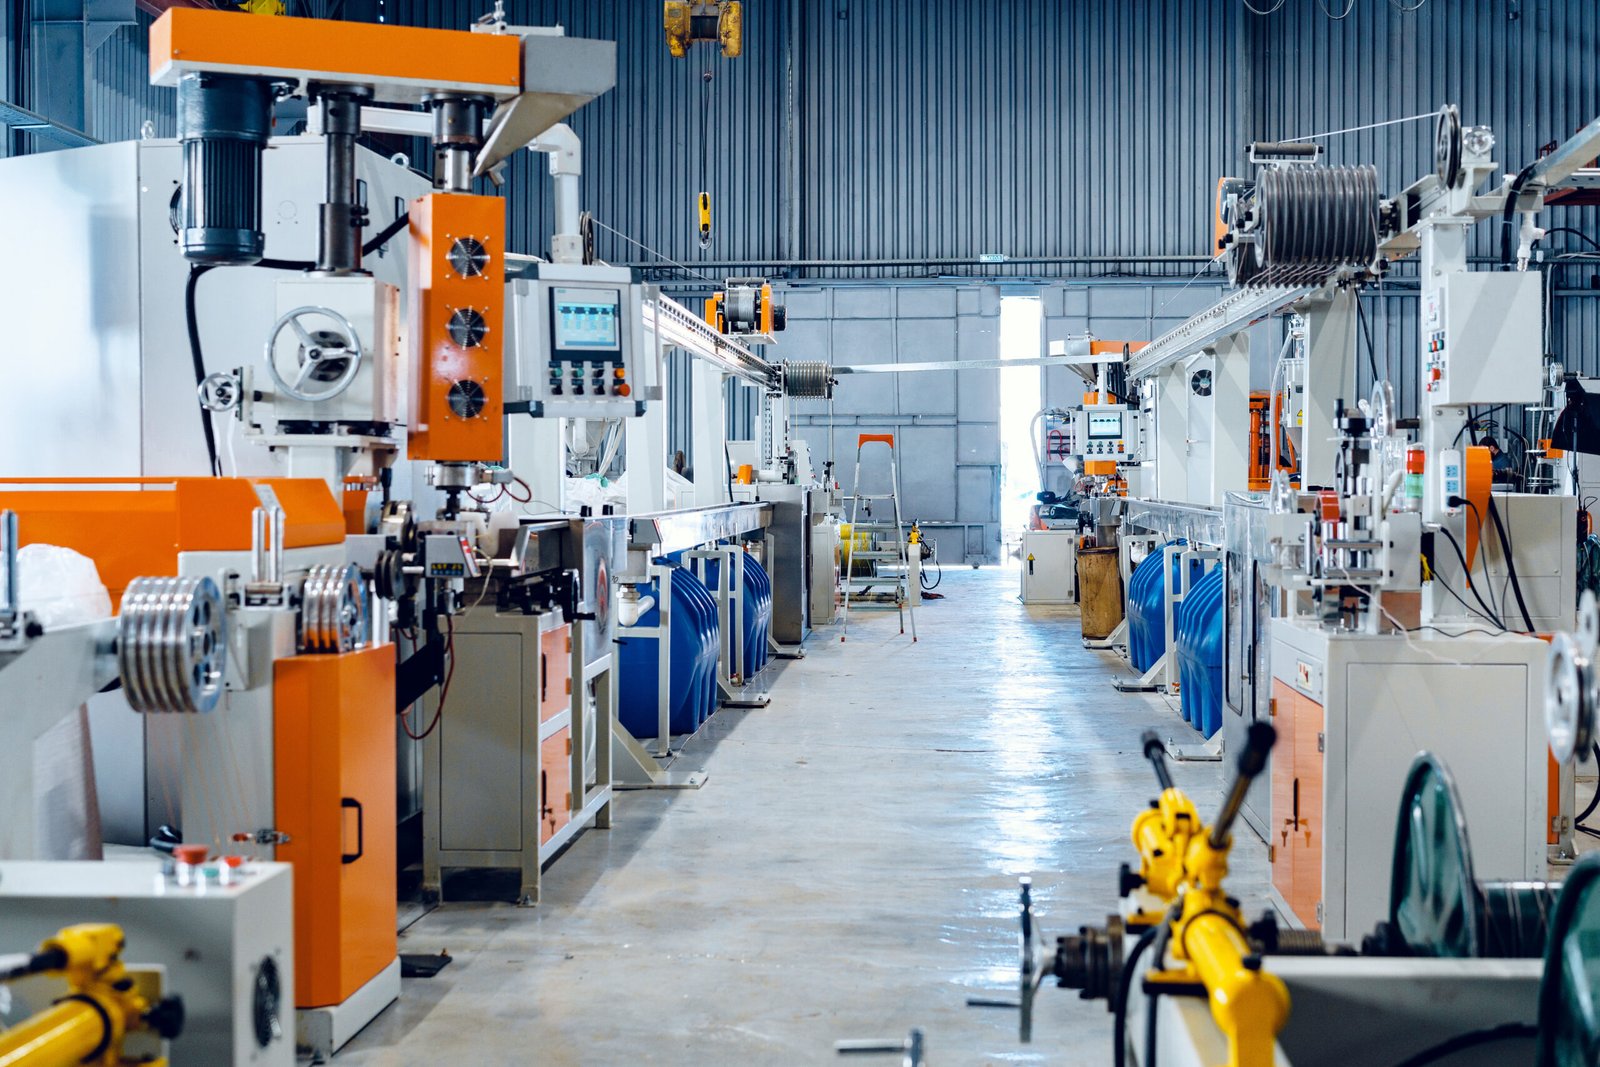
Real HONGKAI workshop image of electrical cable production equipment. It is a machinery reference, not a claim that every low-voltage cable uses the same configuration.
This guide is for factory owners, production managers and technical procurement teams choosing a route for building wire, THHN or THWN, flexible cable or control cable. The decision is not which catalog has the most machines. The decision is which minimum complete route can make the approved product, connect to the factory and produce evidence that the buyer can accept.
What Must Buyers Specify Before Selecting a Low-Voltage Cable Production Line?
A buyer should lock eight decisions before comparing low-voltage cable production line proposals: finished product, acceptance basis, conductor, conductor-forming process, applied materials, core assembly, testing and handling, and factory integration. Each decision changes either the required machine stages or the interfaces between them. HONGKAI should receive the cable drawing and project brief before proposing models because a family name alone does not define the construction. Unconfirmed values should remain marked for project confirmation instead of being copied from another cable.
1. Finished Cable: Which saleable cable must the factory make first?
Why it matters: “Low-voltage cable” is a market category, not a complete production specification. A single insulated building wire may need conductor preparation, insulation, testing and coiling, while a flexible multicore cable can also need fine-wire bunching, core cabling and an outer sheath. A control cable may add shielding or other protection only when the approved design requires it. Selecting every possible stage wastes capital and floor space; omitting one required stage creates an incomplete factory.
질문 항목: 최초로 판매 가능한 케이블의 이름, 명칭, 도체 재질 및 구조, 코어 수, 절연재, 외피, 보호 구조, 완성 직경 또는 승인된 범위, 포장 방식 및 타겟 시장을 명시하십시오. 현재 케이블 도면 또는 측정 가능한 복원 계획이 포함된 승인된 샘플을 첨부하십시오. 사전 HONGKAI 경로 검토를 위해서는 정확한 제품명, 완성 사양 및 가독성 있는 케이블 단면도가 최소한의 시작 조건입니다. 단면도는 제품명이 숨길 수 있는 도체 세부 사항, 코어 수, 적용된 층 및 보호 요소를 드러냅니다. 향후 케이블 패밀리는 별도로 목록화하여 공급업체가 첫날 범위와 선택적 확장 경로를 구분할 수 있도록 하십시오.
How to verify: Trace every layer of the finished cable backward to an incoming material and a manufacturing stage. Use HONGKAI’s low-voltage wire and cable production hub to compare preliminary routes for building wire, THHN or THWN, flexible cable and control cable. Then require the supplier to mark which stages are supplied, integrated from a specialist manufacturer, already owned by the buyer or excluded.
Red flags: The proposal says only “electrical cable line,” uses one machine list for every product family, or adds future products without a drawing, material system or acceptance method.
2. Acceptance Basis: Which document controls the cable design and tests?
Why it matters: A familiar cable name can refer to different construction and marking obligations in different markets. The buyer’s approved standard, drawing and customer specification decide conductor requirements, materials, dimensions, electrical tests, mechanical tests, markings and packaging. Machinery cannot create compliance by itself, and a machine supplier should not promise certification for a cable that has not been defined and tested through the required process.
What to ask: Identify the applicable product standard and edition, customer specification, drawing revision, sampling plan, test methods, pass limits, marking text and certification responsibility. State whether the factory will use an existing approved design or develop a new product that needs qualification. Keep machinery acceptance separate from finished-product certification while connecting the same controlled drawing to both.
How to verify: Build a requirements matrix with one row for each cable characteristic and one column for the document, production control, test method, instrument and retained record. IEC 60228:2023 covers nominal conductor cross-sections, conductor constructions and resistance requirements for a broad range of power cables and cords, but the product-specific standard decides whether and how it applies.1 For PVC-insulated cable families within its scope, IEC 60227-1:2024 supplies general requirements and points to the relevant particular parts and test methods.2
Red flags: The quotation uses “IEC standard” without a number or edition, the supplier selects tests after the machine is built, or a proposed UL mark is treated as a machine feature rather than a finished-product certification responsibility.
3. Conductor Input: What conductor structure enters the insulation stage?
Why it matters: The insulation line sees a physical input, not a marketing name. Solid, stranded and fine-stranded conductors require different upstream preparation, reel formats, tension control and surface-condition checks. A factory that buys ready-to-insulate conductor needs a different project scope from a factory that begins with rod or individual fine wires.
What to ask: Define conductor material, solid or stranded construction, nominal size system, individual-wire data where applicable, compacted or non-compacted form, incoming package, allowable range, joint policy, surface condition and resistance acceptance. State whether drawing, annealing, tinning, bunching or rigid stranding is in the new project, already available in the factory or purchased as prepared conductor.
How to verify: Inspect the approved conductor drawing and a representative incoming reel. Connect each required transformation to a named machine and measurement. For projects that require intermediate copper-wire drawing, use the 중간 와이어 드로잉 머신 레퍼런스 to check the proposed inlet and outlet sizes before selecting upstream and downstream equipment. Confirm the pay-off package, guide path, tension range and downstream insulation interface against the actual conductor, then include the same input in the FAT material list. IEC 60228 relates primarily to the conductor in the finished cable, so the buyer still needs process controls for the intermediate conductor entering production.1 프로젝트에서 도체 준비를 내부에서 수행할 경우, 월간 수요 및 사용 가능한 예산을 준비된 도체 구매와 비교하십시오. 하나의 HONGKAI 프로젝트 사례에서, 월간 수요가 수십 킬로미터에 불과했을 때, 공장이 가동률을 유지할 수 없는 드로잉 및 어닐링 장비를 도입하는 것보다 준비된 도체 구매가 더 실용적이었습니다. 이 사례는 보편적인 기준이 아니며, 결정은 구매자의 실제 제품 혼합, 월간 요구량 및 투자 계획에 따라 달라집니다.
Red flags: The supplier assumes copper when aluminum is possible, assumes a fine-stranded conductor can be handled like a solid conductor, or quotes a buncher without the individual-wire, finished-conductor and package definitions.
4. Conductor Forming: Does the route require bunching or stranding?
Why it matters: Bunching and ordered stranding are not interchangeable labels. The approved conductor construction, individual-wire input, finished size, lay requirements, package and downstream use decide the process. Flexible conductors commonly require a bunching stage, while other low-voltage power conductors may require a different stranding method; a solid conductor needs neither.
What to ask: Specify the individual-wire count and range, finished conductor construction, lay direction and required lay range, finished package, conductor test plan and intended insulation line. Ask whether the machine forms bare conductor, insulated cores or both, because those are different production tasks. Request a machine configuration tied to the exact input and output rather than to the largest model in a series.
How to verify: Run the agreed conductor using the specified pay-off and take-up packages, then verify the finished construction, dimensions, resistance and downstream handling by the project method. HONGKAI’s wire bunching machine reference shows that model selection changes with conductor input, finished size, lay range and package. The double-twist bunching machine reference is a separate equipment family and should be reviewed against the same approved conductor data.
Red flags: A proposal uses “stranding machine” without naming the process, quotes a maximum speed without the conductor and package, or cannot show how the finished conductor will feed the insulation stage.
5. Applied Layers: Which insulation and outer coverings must the line apply?
Why it matters: Material names alone do not define an extrusion process. The approved compound grade, conductor, layer construction, thickness controls, cooling route, marking method and finished handling determine the extruder, crosshead, tooling and auxiliary scope. THHN or THWN also should not be reduced to “ordinary PVC wire” because the designation and construction include specific marking and evaluation requirements.
질문 항목: 승인된 등급별 절연재 및 외피 재질, 층 순서, 명목 및 최소 두께 규정, 색상 계획, 지정된 경우 도체 사전 가열 요구사항, 표면 마감, 동심도 측정 방법, 스파크 테스트 요구사항, 인쇄 레전드, 냉각 한계 및 완성 포장을 제공하십시오. 다층 구조의 경우, 각 층이 승인된 공정에 따라 병렬 적용, 공공사출 또는 별도 공정으로 제작되는지 명시하십시오. HONGKAI THHN 또는 THWN 구성 검토의 경우, “PVC 플러스 나일론”은 완전한 입력이 아닙니다. 정확한 제품 구조, 요구 인쇄, 완성 포장 및 의도된 케이블 테스트도 적용, 마킹, 테스트 및 취급 보조 장치를 사출 범위와 일치시키기 위해 필요합니다.
How to verify: Review the cable cross-section and bill of materials with the tooling and auxiliary list. Challenge the proposal against every layer and require samples tied to the material lot, recipe, line condition and test results. The UL Solutions Wire and Cable Application Guide explains that THHN identifies thermoplastic insulation for dry use with a nylon jacket and that wire designations communicate intended use and evaluated characteristics.3 The buyer must still provide the exact product and certification basis for the target market.
Red flags: The machine list does not name how a nylon or other outer layer is applied, compound compatibility is assumed from a generic polymer name, or the supplier presents a cable designation as proof that the proposed line can meet it.
6. Core Assembly: Does the cable need cabling, shielding or an outer sheath?
Why it matters: An insulated single conductor can leave the extrusion stage as a finished product, but a flexible or control cable usually continues through additional assembly. Core count, lay, fillers, binders, identification, shield construction and outer sheath create new tension zones, pay-offs, tooling and acceptance checks. These stages must be mapped from the approved cable drawing rather than copied from a power-cable template.
What to ask: Define core count and identification, cabling lay, direction, filler and binder, shield material and coverage method when required, drain wire if specified, separator, inner covering and outer sheath. State which stages occur online and which are separate operations. Specify the reel presented by the insulation stage and the reel required by cabling or sheathing equipment.
확인 방법: 층별 공정 맵을 작성하고 절연 코어에서 완성 케이블까지 재료 흐름을 추적하십시오. 지정된 모든 페이아웃 위치, 장력 인터페이스, 가이드, 바인더, 쉴드 공급, 캡스탄 및 테이크업을 프로젝트 도면과 비교하십시오. 표시된 모든 층을 필수 공정 입력으로 처리하십시오. 지정된 쉴드는 해당 쉴딩 공정이 필요하고, 많은 미세 선으로 구성된 도체는 적절한 버칭 공정이 필요하며, 여러 절연 코어는 케이블링이 필요하고, 외부 화합물 층은 쉬싱이 필요합니다. 따라서 단일 쉬싱과 이중 쉬싱 구조가 동일한 최종 구성으로 간주될 수 없습니다. HONGKAI 저전압 경로는 쉴딩 및 보호를 조건부 공정으로 처리하며, 확인된 제어 케이블 설계에서 필요할 때만 범위에 포함됩니다.
Red flags: The proposal assumes every control cable is shielded, uses one cabling arrangement for different core counts without review, or omits the reel and tension interface between core insulation and final assembly.
7. Testing and Handling: How will the factory prove and package the product?
Why it matters: A production route is incomplete if the factory can extrude cable but cannot measure, test, identify and package it as the approved product. Online checks support process control; routine and final tests support release. Coiling and reel handling also change with product dimensions, package rules, batch length and customer presentation.
What to ask: Define online diameter or other required gauges, spark testing where applicable, length measurement, print verification, conductor resistance, voltage or other product tests, sampling frequency, laboratory instruments, traceability fields, coil or reel format, standard length, wrapping, labeling and pallet requirements. State which instruments belong online, in a routine-test area or in the final laboratory.
확인 방법: 원료 식별에서부터 레시피, 온라인 기록, 오프라인 테스트 결과 및 완성 라벨까지 하나의 FAT 샘플을 추적하십시오. 라인 카운터를 승인된 길이 검증 방법과 비교하십시오. 대상 포장에서 코일 또는 릴 품질을 검사하고, 다음 처리 단계가 케이블을 손상시키거나 추적 가능성을 흐리지 않는지 확인하십시오. 장비 공유는 제품별로 구성을 특화하므로, FAT은 대상 케이블 사양에서 구축하십시오. 무하중 회전 테스트는 최종 제품 수락이 아닙니다. 기록은 승인된 제품 사양, 테스트된 장비 구성, 식별된 샘플 및 측정 결과를 연결해야 합니다.
경고 신호: 견적은 풀림 장치에서 끝나며, 테스트 장비는 방법이나 범위 없이 나열되어 있으며, 포장 요구사항은 FAT 이후에야 나타나거나, 샘플 라벨이 생산 및 테스트 기록과 연결되지 않습니다.
8. 공장 통합: 모든 필요한 단계가 하나의 통제된 공정으로 운영될 수 있습니까?
중요한 이유: 올바른 장비라도 포장, 라인 방향, 유틸리티, 바닥 면적, 제어 책임 및 재료 흐름이 연결되지 않으면 열악한 프로젝트가 됩니다. 생산 매니저는 운영자가 실행하고, 정비 인력이 접근하며, 품질 인력이 감사할 수 있는 공정이 필요합니다. 기존 장비와 계획된 확장은 레이아웃상의 빈 공간이 아니라 실제 인터페이스로 처리되어야 합니다.
질문할 내용: 공장 레이아웃, 사용 가능한 바닥 면적, 접근 및 리프팅 경로, 전력 및 접지 데이터, 냉각 및 압축 공기 조건, 배수, 환기, 원자재 보관, 공정 중 제품 이동 경로, 실험실 위치, 기존 장비, 정비 여유 공간, 인력 계획 및 확장 경계를 제공하세요. HONGKAI-제조 장비, 전문 시스템, 구매자 제공 항목 및 현장 작업을 모두 포함하는 하나의 책임 매트릭스를 요청하세요.
확인 방법: 구성이 고정되기 전에 전체 레이아웃 및 유틸리티 매트릭스를 검토하십시오. 입력 도체에서 완성 포장까지 릴 이동을 추적하고 모든 수동 이전을 기록하십시오. 릴링 전후 직경, 코어 수, 사출 전후 직경 및 모든 결과가 선택된 장비의 승인된 가공 범위 내에 유지되는지를 기록하는 직경-포장 인터페이스 시트를 추가하십시오. 케이블 직경, 필요한 릴 크기 및 상업 계획을 기반으로 각 테이크업을 선택하되, 공장이 생산 릴을 직접 판매하는지 또는 케이블을 더 작은 판매 포장으로 전환하는지도 포함하십시오. 정상 생산 중에도 정비 접근로, 작업자 통로, 안전 구역 및 실험실 샘플링이 사용 가능함을 확인하십시오. 개별 장비 시연을 수용하는 대신, 인터페이스에 대해 하나의 연결된 FAT 및 현장 수락 매트릭스를 사용하십시오.
경고 신호: 레이아웃은 주문 후에 만들어지며, 보조 시스템에 명시된 공급업체가 없고, 포장이 처리 장비 없이 단계마다 변경되거나, 유틸리티가 단순히 “표준 공장 공급”으로만 설명됩니다.”
참고: 저전압 케이블 생산 라인은 모든 층, 변환, 인터페이스 및 수용 기록이 승인된 완성 케이블로까지 추적 가능할 때만 선택 가능합니다.
빌딩 와이어, THHN, 유연 케이블 및 제어 케이블 경로는 어떻게 다릅니까?
빌딩 와이어, THHN 또는 THWN, 유연 케이블 및 제어 케이블은 하나의 보편적 라인으로 처리하는 것이 아니라 네 가지 기준 경로로 처리해야 합니다. 빌딩 와이어는 도체 준비, 절연, 테스트 및 코일링으로 마무리될 수 있으며, THHN 또는 THWN은 승인된 구조에 필요한 층과 제어를 추가합니다. 유연 케이블은 보통 미세선 뭉치를 추가하며, 케이블링 및 쉬싱을 추가할 수도 있고, 제어 케이블은 다중 코어 조립을 추가하며 설계에 표시된 차폐 또는 보호만 추가합니다. HONGKAI는 완성 케이블 도면에서 각 경로를 매핑하고 조건부 단계를 별도로 표시합니다.
| 참조 케이블 | 예비 생산 경로 | 범위를 변경하는 구매자 결정 | 보관할 증거 |
|---|---|---|---|
| 빌딩 와이어 | 준비된 도체 → 절연 → 마킹 및 테스트 → 코일링 또는 리일링 | 고체, 뭉친 또는 유연한 도체; 절연 시스템; 단일 패스 또는 추가 코팅 | 도체 기록, 재료 로트, 치수, 전기 테스트, 인쇄 및 포장 기록 |
| THHN / THWN | 승인된 도체 → 열가소성 절연 → 나일론 또는 승인된 외층 → 마킹, 테스트 및 포장 | 정확한 명칭, 시장 표준, 층 방법, 마킹 및 인증 책임 | Controlled drawing, compound approvals, layer measurements, test and certification records |
| Flexible cable | Fine-wire preparation → bunching → core insulation → cabling when multicore → sheath when required → testing and handling | Strand construction, flexibility requirement, core count, cabling lay and sheath | Finished-conductor data, core identity, cabling and sheath records, final tests |
| Control cable | Conductor preparation → core insulation → multicore cabling → shielding or protection if specified → sheath → testing and handling | Core count, identification, shield construction, drain or binder, protection and installation environment | Core map, lay and shield evidence, sheath data, electrical tests and final label |
These routes are deliberately preliminary. A building wire made from prepared conductor may not need drawing or bunching in the new factory. A flexible single-core product may not need a cabling stage. A control cable without a shield should not receive shielding equipment merely because another control-cable design uses it.
The same discipline applies to machine-source claims. HONGKAI’s current low-voltage hub identifies selected core extrusion equipment as HONGKAI-manufactured and marks specialist machinery separately. The buyer should require that attribution in the technical offer, along with the interface owner, documents, FAT responsibility, spare-parts source and after-sales route for each supplied stage. HONGKAI’s cable machinery spare-parts page provides the identification path for replacement enquiries, but the project should still attach an initial parts list tied to the final equipment configuration.
Note: The product family narrows the process route, but the approved drawing decides which stages are mandatory, conditional or excluded.
What Evidence Should Be Written into the RFQ and FAT Plan?
The RFQ should describe the input, transformation, output and acceptance evidence for every required stage. The supplier should return a compliance matrix, equipment list, source attribution, interface schedule and FAT plan tied to the same cable drawing. HONGKAI machine references can support the preliminary configuration, but exact models, ranges, speeds, utilities and tests remain project-specific until the materials and product requirements are confirmed. A buyer should reject any value that cannot be traced to a stated operating condition and test method.
The following checklist turns the article into a procurement brief:
- ☐ Finished-cable drawing, designation, target market and controlled revision
- ☐ Product standard, customer specification, test methods and certification responsibility
- ☐ Conductor material, construction, size system, input package and acceptance data
- ☐ 요구되는 도면, 완화, 주석 도금, 뭉치기 또는 래싱 공정
- ☐ 승인된 절연재, 외피, 쉴드, 바인더, 필러 및 외피 재질
- ☐ 층 순서, 치수, 색상, 마킹 및 표면 요구사항
- ☐ 코어 수, 식별, 케이블 레이 및 조건부 보호 공정
- ☐ 온라인 검사, 정기 시험, 최종 시험, 샘플링 및 추적 가능성
- ☐ 코일 또는 리ール 형식, 표준 길이, 포장, 라벨 및 팔레트 요구사항
- ☐ 기존 장비, 라인 방향, 패키지 전이 및 확장 경계
- ☐ 레이아웃, 유틸리티, 안전 인터페이스, 정비 접근성 및 인력
- ☐ 장비 출처, 공급 범위, 제외 항목 및 인터페이스 책임
- ☐ FAT 재질, 운전 조건, 안정화 규칙, 샘플 및 합격 기준
- ☐ 매뉴얼, 도면, 제조 공정, 교육, 초기 스페어 및 지원 인수
RFQ은 능력 검토와 보증을 구분해야 합니다. 공급업체는 한 기계 시리즈가 입력 및 출력 범위에 맞게 구성될 수 있음을 보여줄 수 있지만, 최종 제안서에는 정확한 프로젝트 조건이 명시되어야 합니다. 카탈로그 최대 속도는 구매자의 도체, 화합물, 층 구조 및 포장에 대한 안정적인 생산을 증명하지 않습니다. 용량은 모든 필요한 단계에서 균형을 이루어야 하며, 합의된 생산 증거를 통해 확인되어야 합니다.
새 공장을 위한 경우, 완성된 체크리스트와 도면을 HONGKAI을 통해 전송하세요. 프로젝트 문의 페이지. For an expansion project, add nameplates, manuals, reel drawings, line direction, control interfaces and stable production records from the existing equipment. That evidence allows HONGKAI to separate replacement, integration and new-equipment scope without assuming that every existing asset is compatible. For a budget-limited new factory, HONGKAI’s project review first maps the cable specifications supported by current orders. Named cable families planned for roughly the next one to two years can then be reviewed as an expansion route, provided the additional compatibility does not add disproportionate cost and the initial layout preserves practical space and access for the specified future machines.
참고: 강력한 견적은 장비 목록이 가장 긴 것이 아니라, 공장이 판매하려는 케이블과 입력, 출력, 인터페이스, 수락 증거가 일치하는 가장 짧은 완전한 경로입니다.
-
IEC 60228:2023, 절연 케이블의 도체. 공식 IEC 페이지는 도체 단면, 구조 및 저항 요구사항을 설명하며, 제품별 표준이 적용 여부를 결정한다고 명시합니다.↩ ↩
-
IEC 60227-1:2024, 등급 전압이 450/750 V 이하인 폴리염화비닐 절연 케이블 — 제1부. 공식 IEC 페이지는 특정 케이블 유형에 필요한 일반 범위 및 특정 부문과 시험 방법을 식별합니다.↩
-
UL Solutions Wire and Cable Application Guide. 공식 가이드는 와이어 표기, 마킹 및 제품 식별, 사용 목적, 인증 증거 간의 관계를 설명합니다.↩



