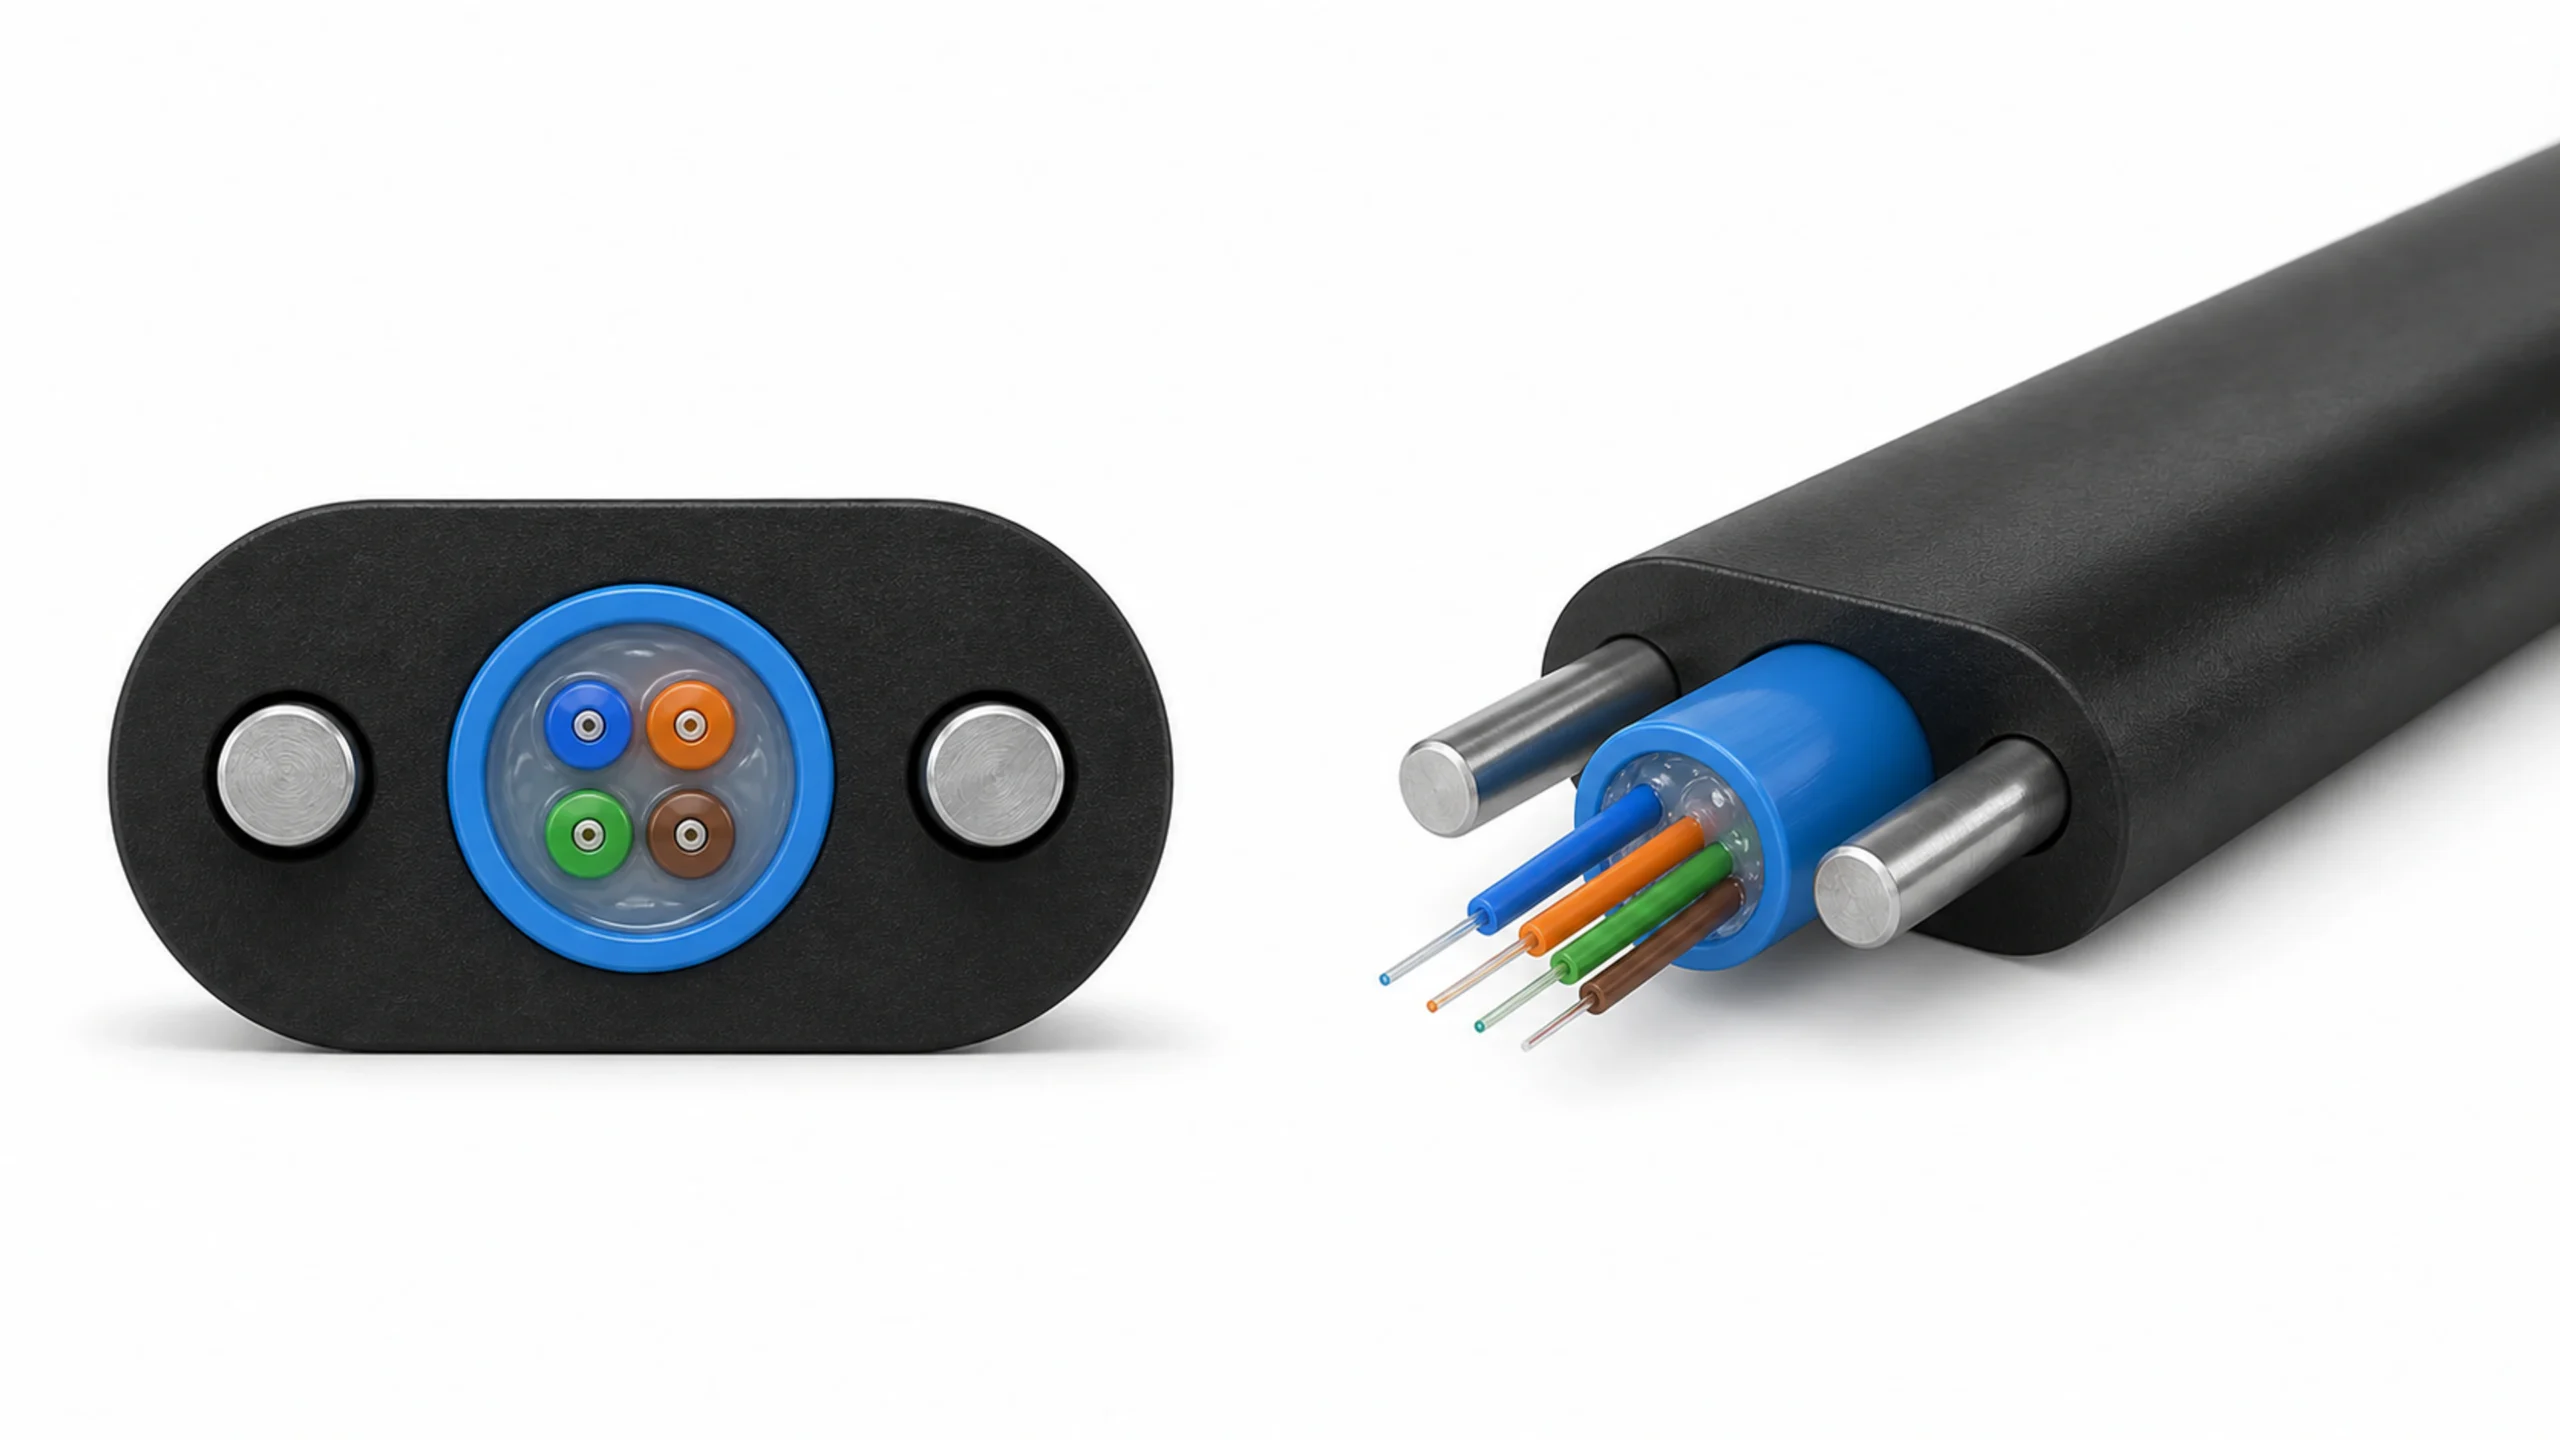
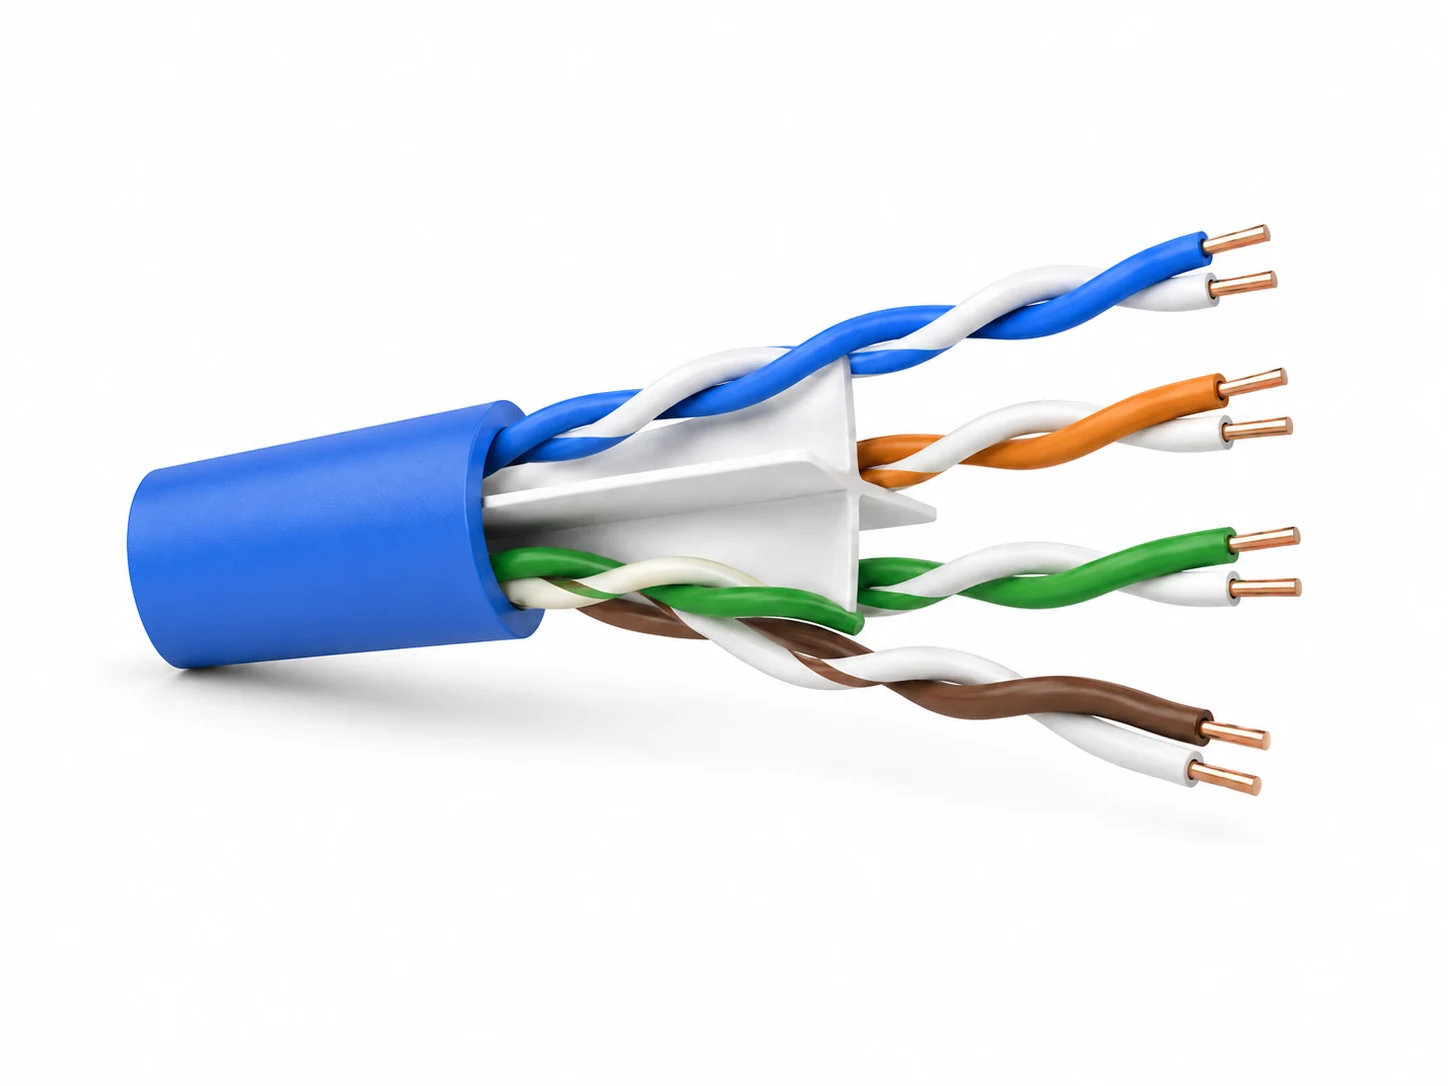
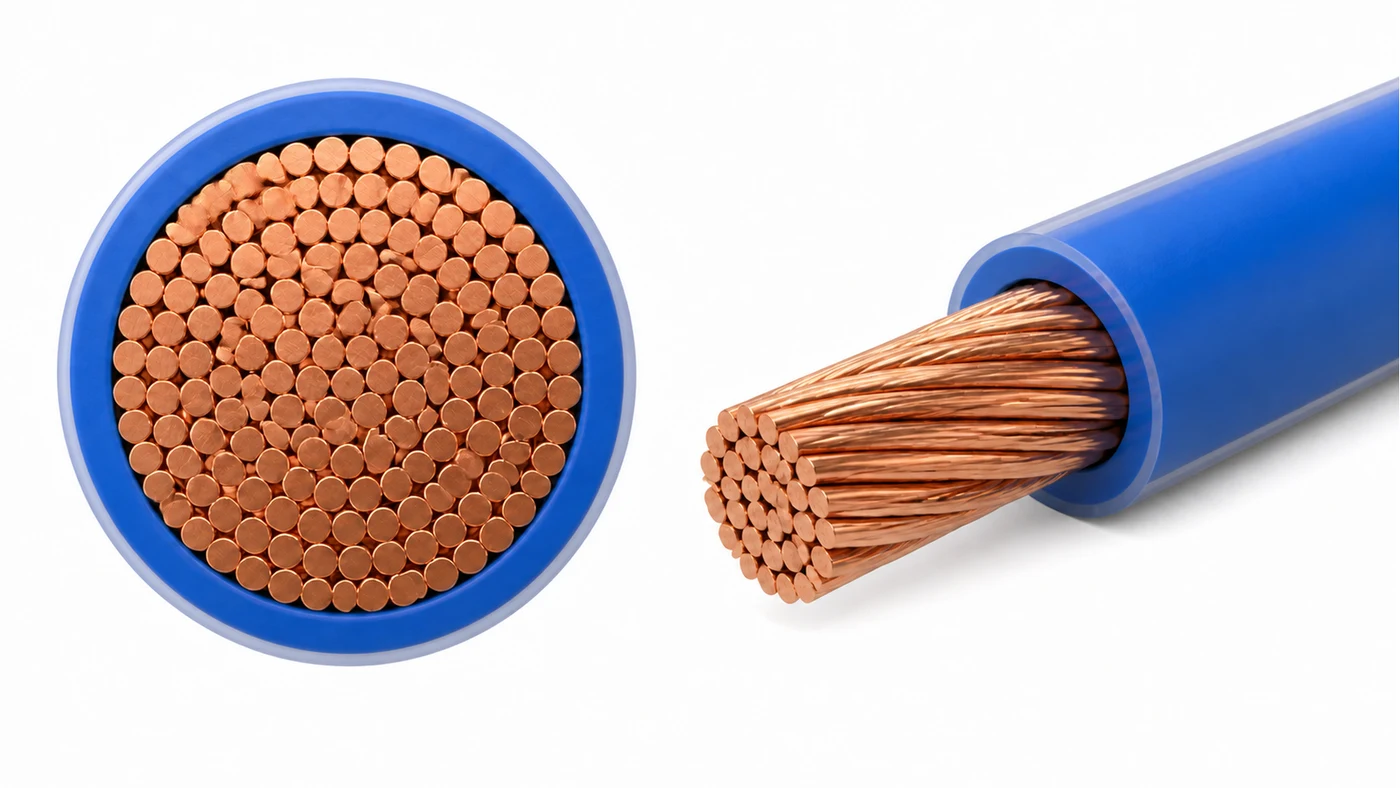
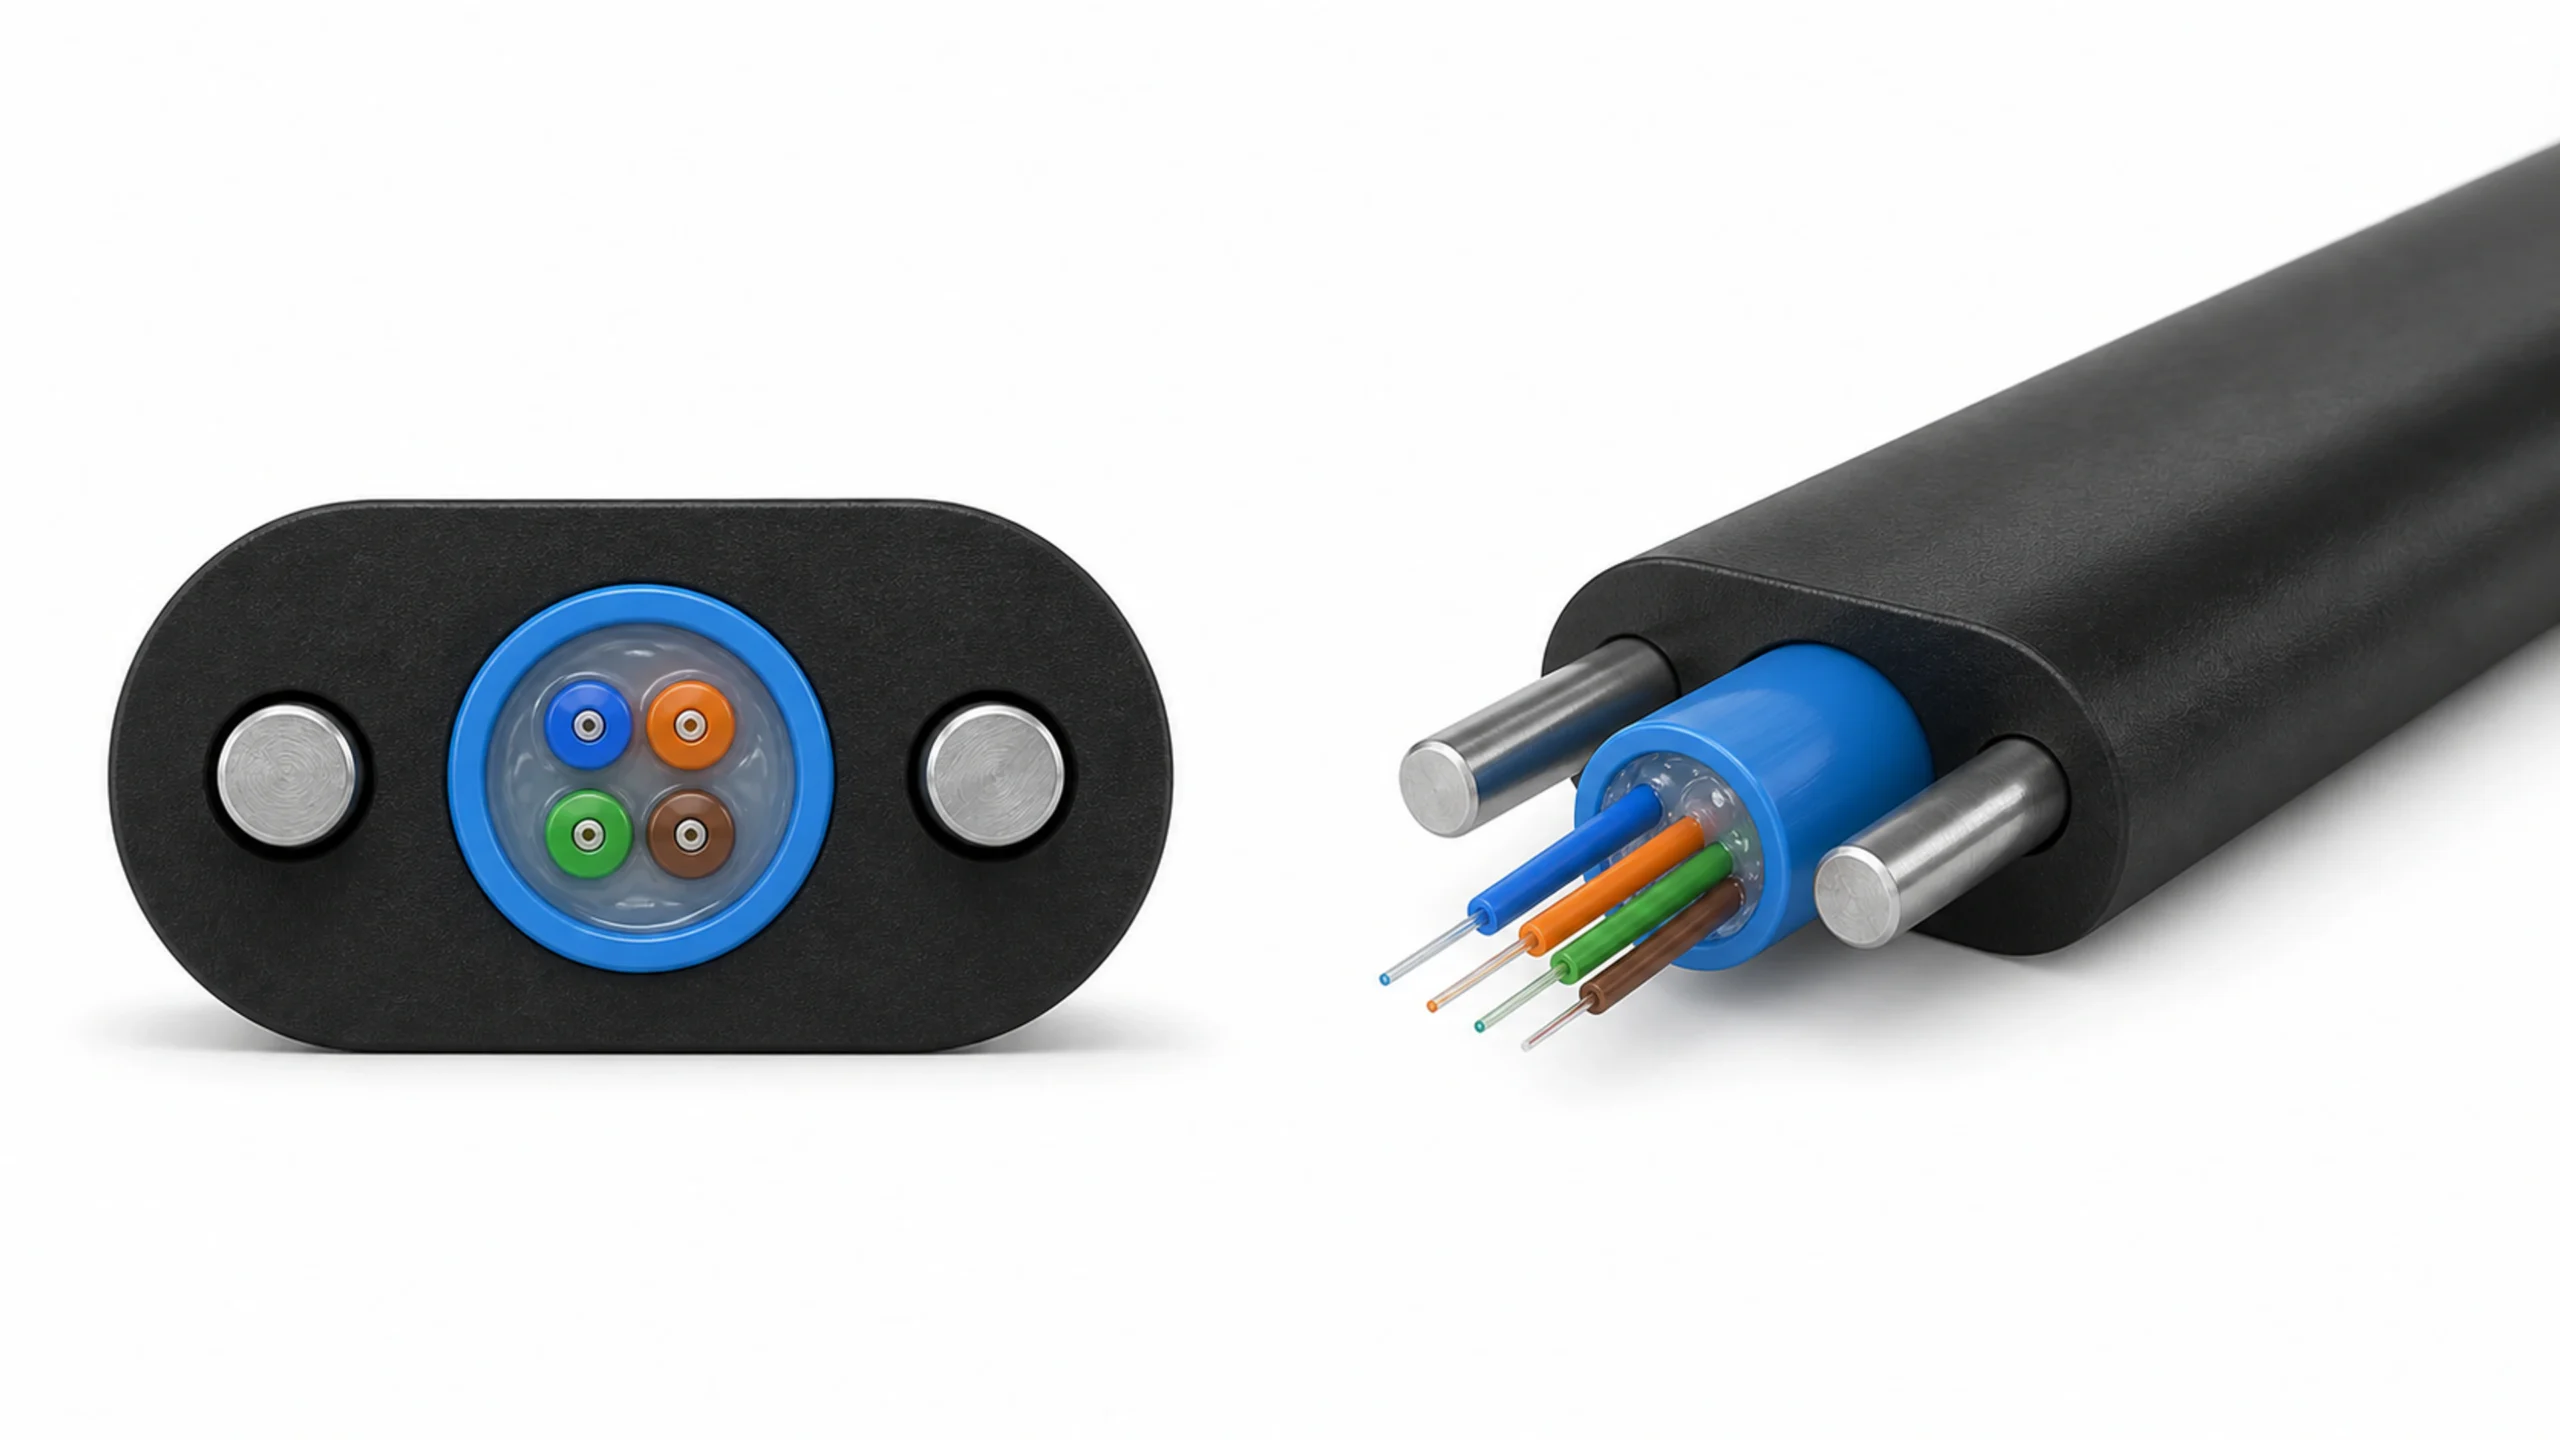
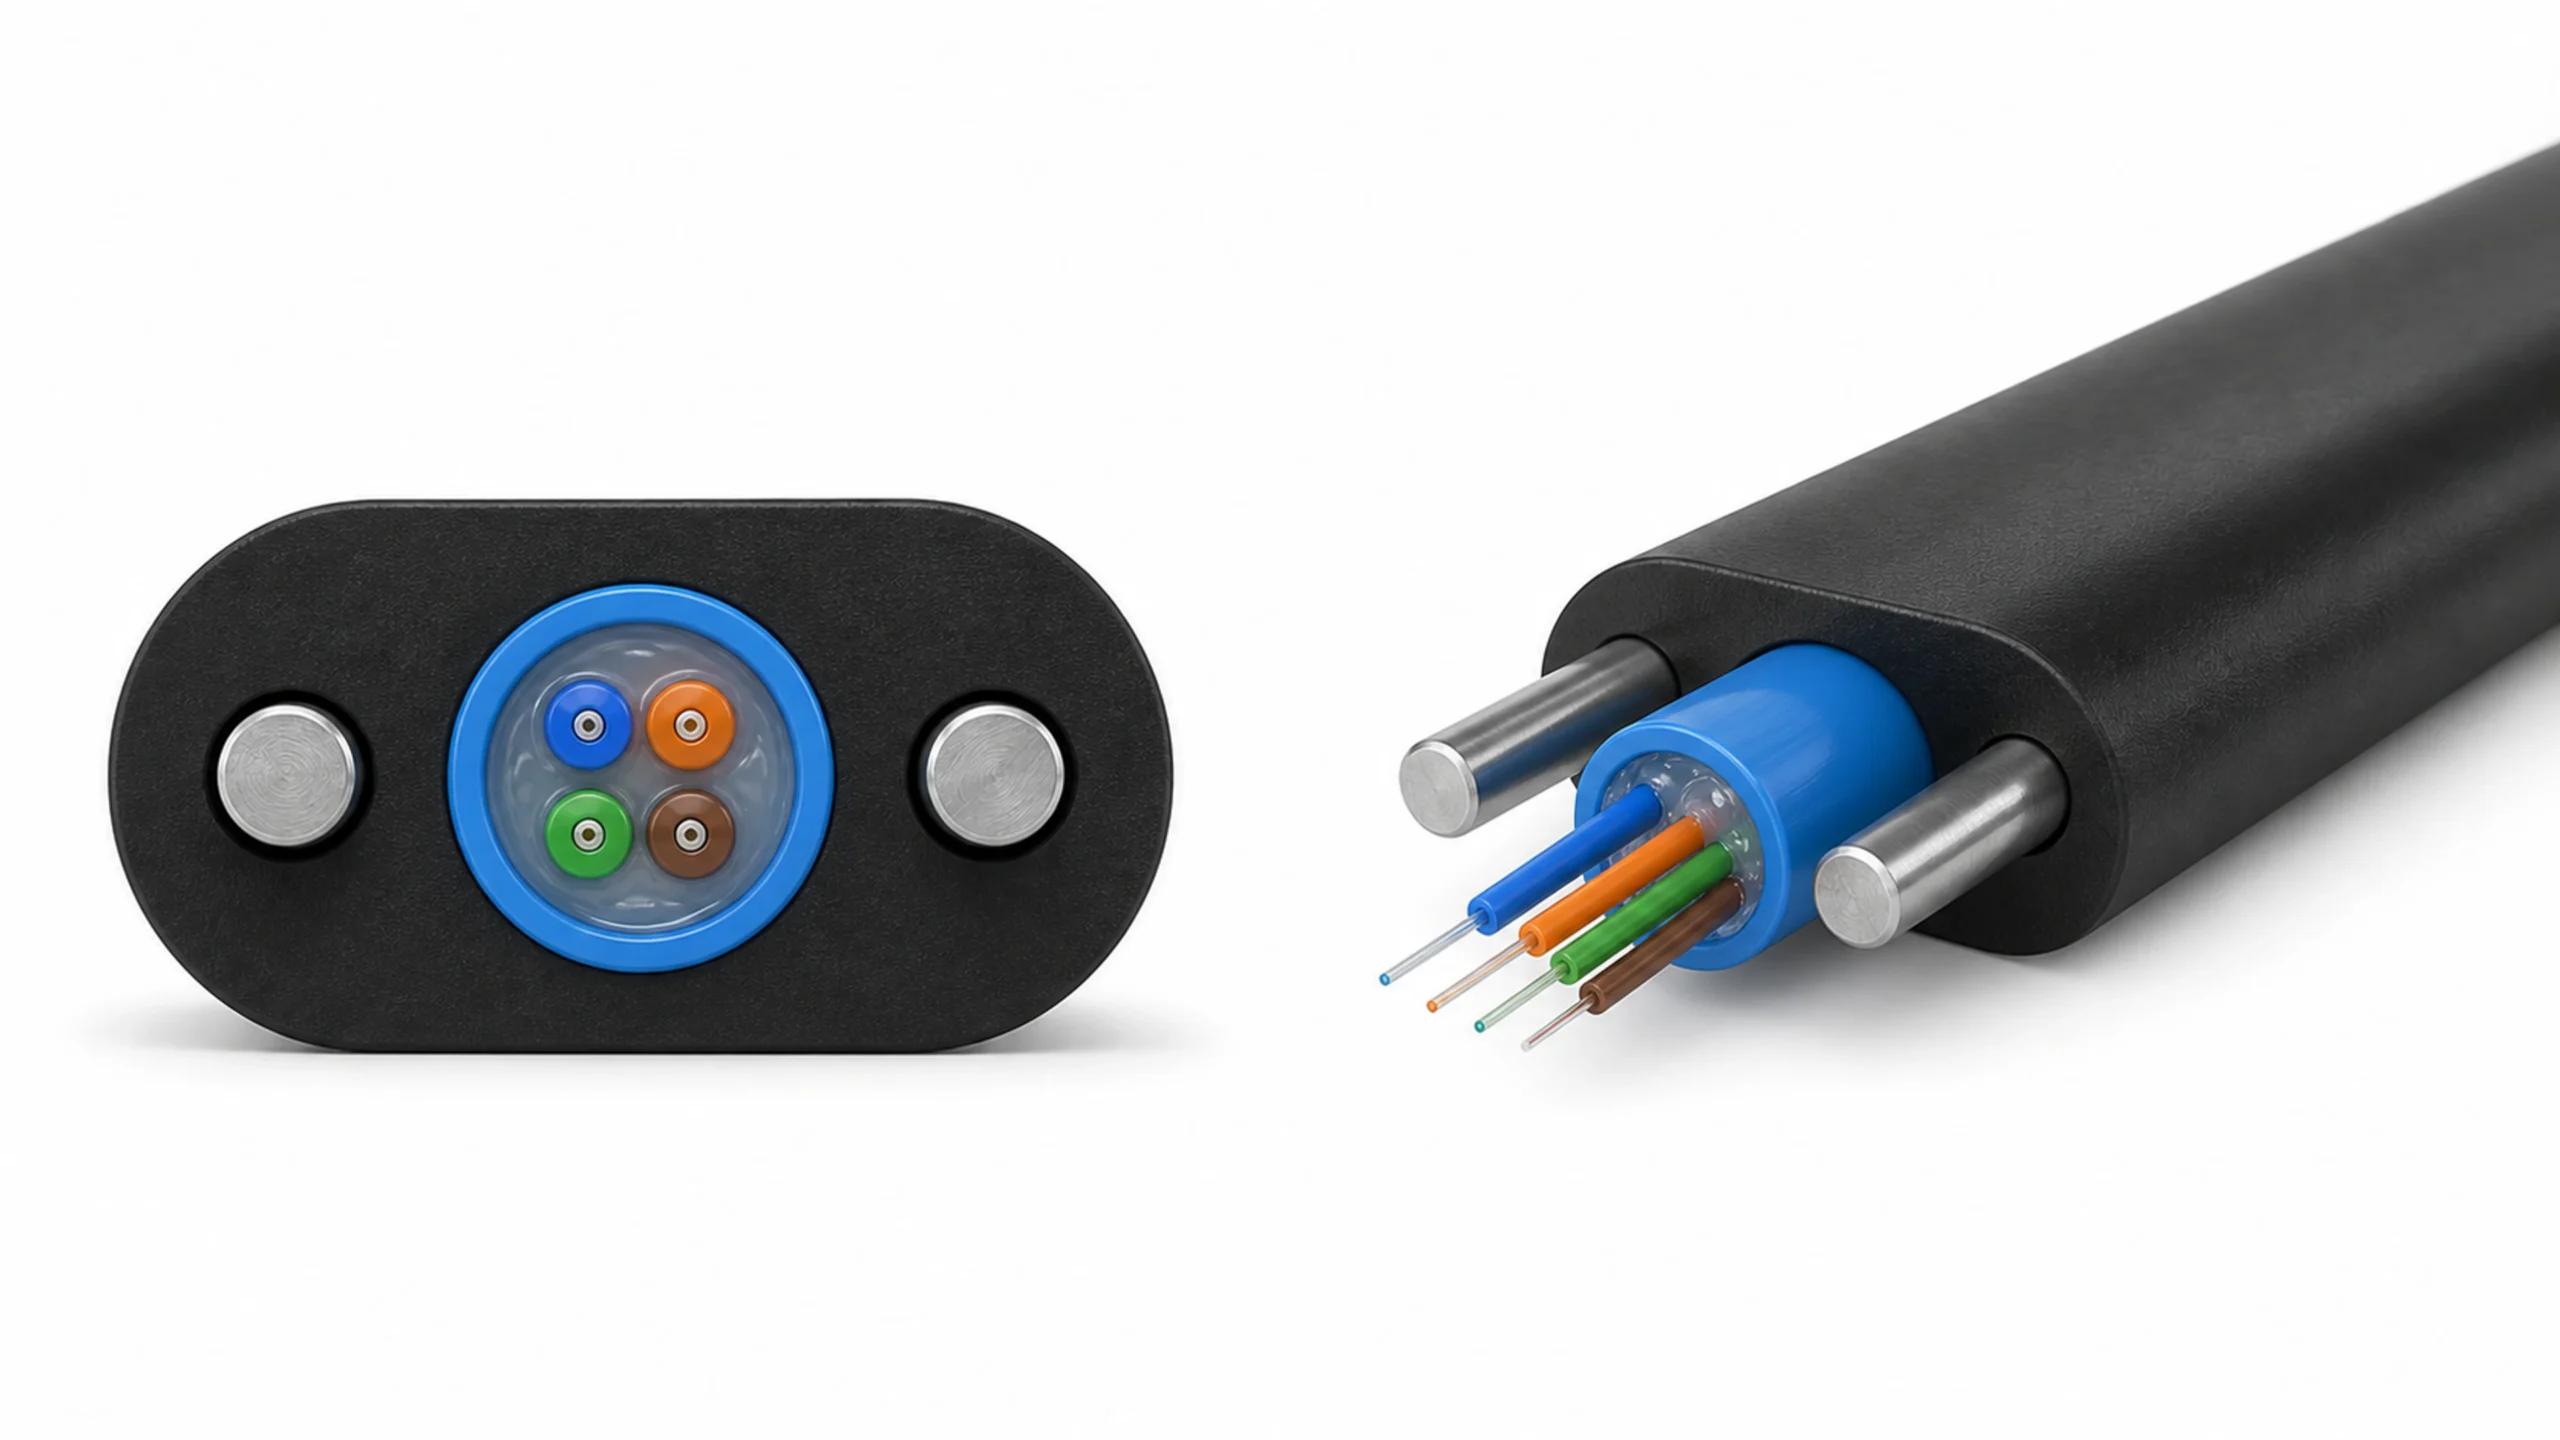



A low-voltage cable factory owner should not start an equipment enquiry with a generic request for “one cable line.” Building wire, THHN or THWN, flexible cable and control cable can share some processes, but their conductor construction, applied layers, core assembly, testing and finished handling create different production routes.
The correct low-voltage cable production line starts with one approved finished-cable design, not a machine model. A buyer should define the conductor, insulation and covering layers, number of cores, protection elements, target package and acceptance basis before equipment is selected. Only the required stages should enter the project scope, and every interface between those stages should be written into the quotation and factory acceptance test. HONGKAI can then map the confirmed design to a project-specific combination of conductor preparation, bunching or stranding, extrusion, assembly, testing and handling equipment.
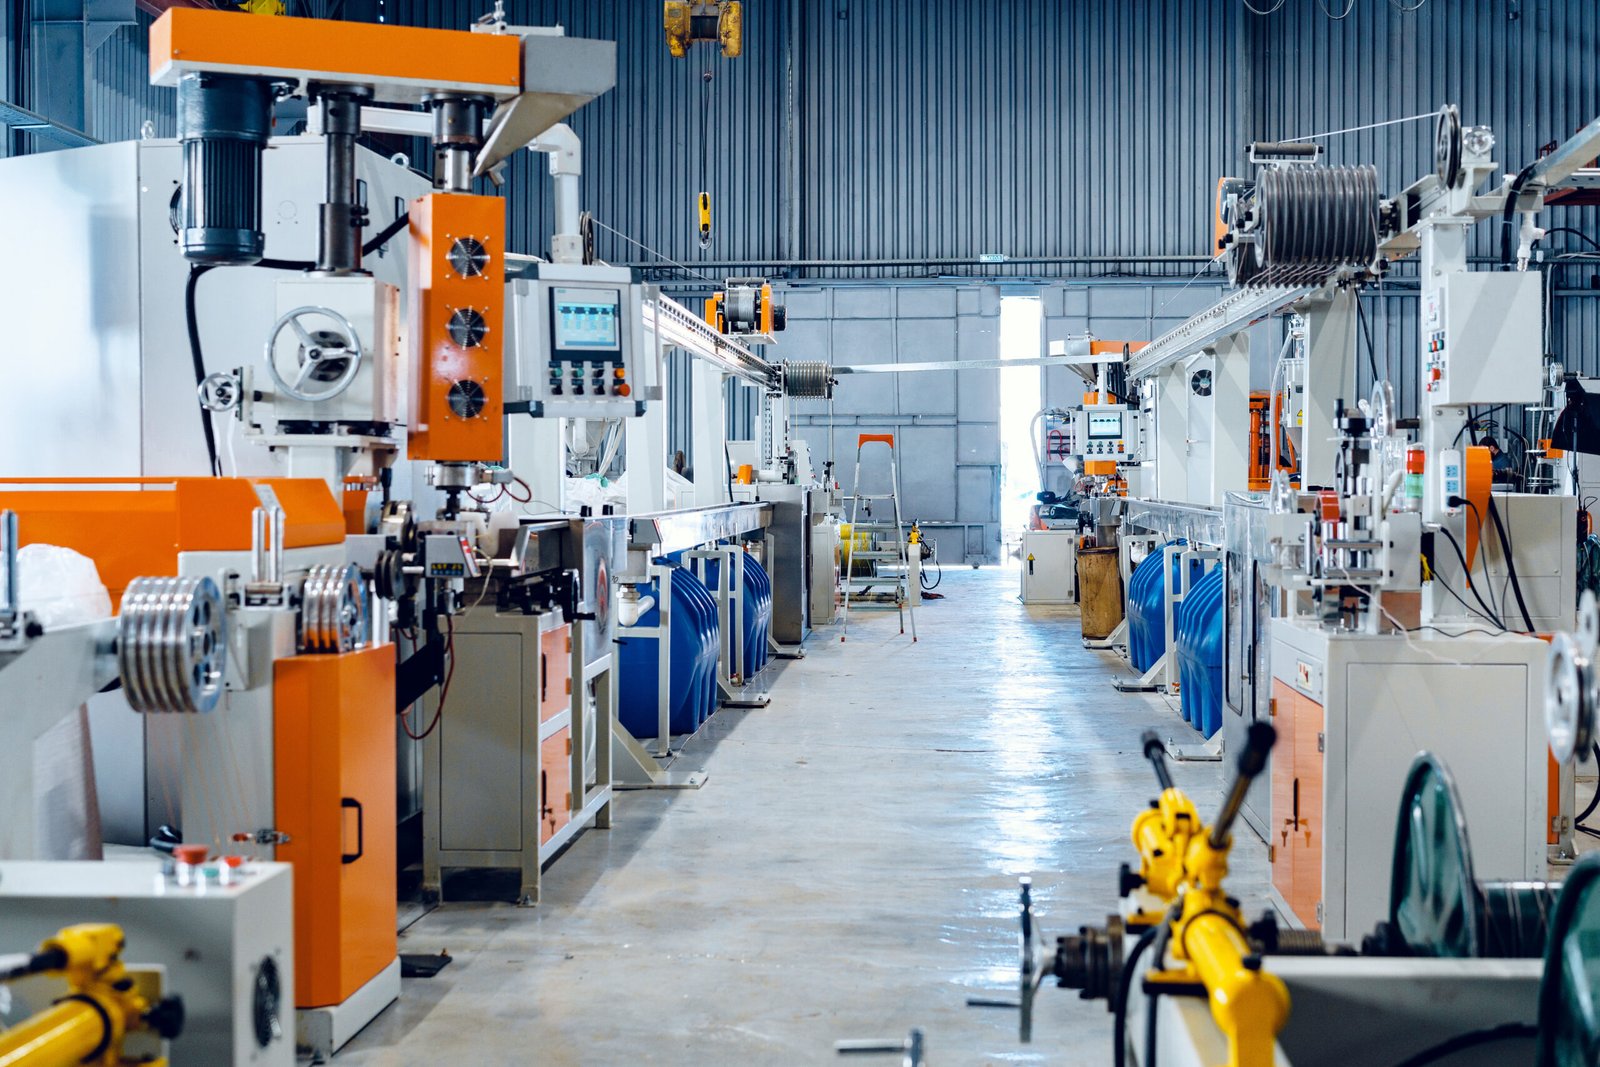
Real HONGKAI workshop image of electrical cable production equipment. It is a machinery reference, not a claim that every low-voltage cable uses the same configuration.
This guide is for factory owners, production managers and technical procurement teams choosing a route for building wire, THHN or THWN, flexible cable or control cable. The decision is not which catalog has the most machines. The decision is which minimum complete route can make the approved product, connect to the factory and produce evidence that the buyer can accept.
What Must Buyers Specify Before Selecting a Low-Voltage Cable Production Line?
A buyer should lock eight decisions before comparing low-voltage cable production line proposals: finished product, acceptance basis, conductor, conductor-forming process, applied materials, core assembly, testing and handling, and factory integration. Each decision changes either the required machine stages or the interfaces between them. HONGKAI should receive the cable drawing and project brief before proposing models because a family name alone does not define the construction. Unconfirmed values should remain marked for project confirmation instead of being copied from another cable.
1. Finished Cable: Which saleable cable must the factory make first?
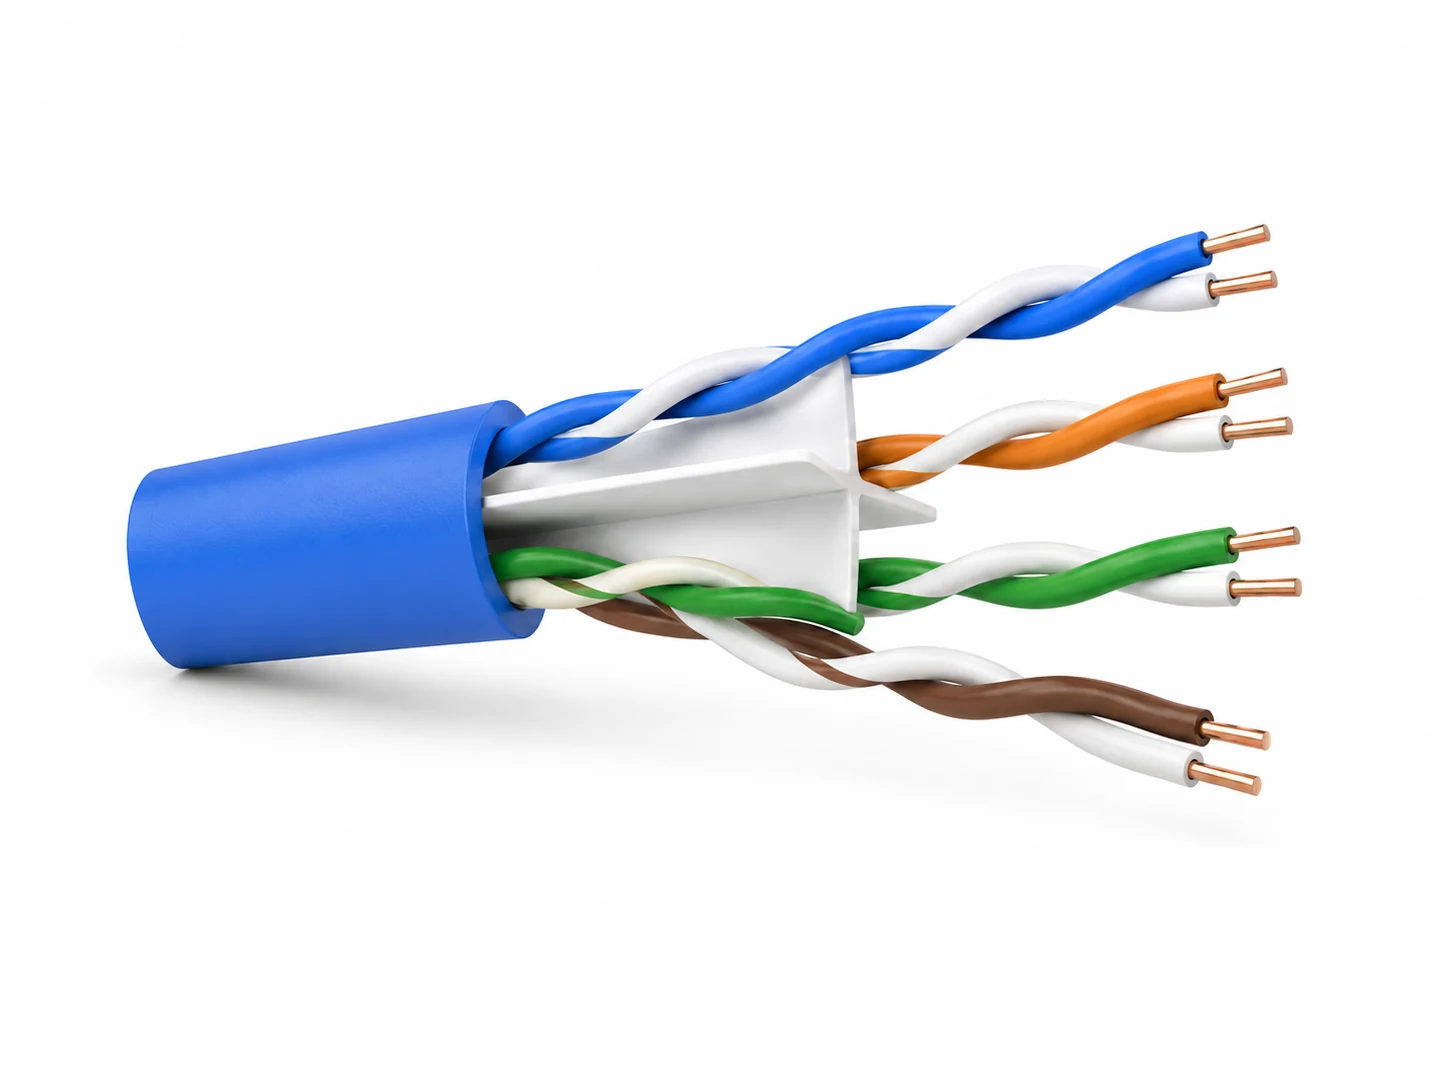
Why it matters: “Low-voltage cable” is a market category, not a complete production specification. A single insulated building wire may need conductor preparation, insulation, testing and coiling, while a flexible multicore cable can also need fine-wire bunching, core cabling and an outer sheath. A control cable may add shielding or other protection only when the approved design requires it. Selecting every possible stage wastes capital and floor space; omitting one required stage creates an incomplete factory.
Yang harus ditanyakan: Sebutkan kabel pertama yang dapat dijual, mencakup penunjukannya, bahan dan struktur konduktornya, jumlah inti, isolasi, selubung luar, konstruksi pelindung, diameter jadi atau rentang yang disetujui, kemasan, serta pasar target. Lampirkan gambar kabel terkini atau contoh yang telah disetujui beserta rencana rekonstruksi yang dapat diukur. Untuk tinjauan awal rute HONGKAI, nama produk pasti, spesifikasi jadi, dan penampang melintang kabel yang dapat dibaca merupakan set minimum untuk memulai; penampang melintang tersebut memperlihatkan detail konduktor, jumlah inti, lapisan-lapisan yang diterapkan, serta elemen pelindung yang mungkin disembunyikan oleh nama keluarga produk. Cantumkan keluarga kabel mendatang secara terpisah agar pemasok dapat membedakan cakupan hari pertama dari jalur ekspansi opsional.
How to verify: Trace every layer of the finished cable backward to an incoming material and a manufacturing stage. Use HONGKAI’s low-voltage wire and cable production hub to compare preliminary routes for building wire, THHN or THWN, flexible cable and control cable. Then require the supplier to mark which stages are supplied, integrated from a specialist manufacturer, already owned by the buyer or excluded.
Red flags: The proposal says only “electrical cable line,” uses one machine list for every product family, or adds future products without a drawing, material system or acceptance method.
2. Acceptance Basis: Which document controls the cable design and tests?
Why it matters: A familiar cable name can refer to different construction and marking obligations in different markets. The buyer’s approved standard, drawing and customer specification decide conductor requirements, materials, dimensions, electrical tests, mechanical tests, markings and packaging. Machinery cannot create compliance by itself, and a machine supplier should not promise certification for a cable that has not been defined and tested through the required process.
What to ask: Identify the applicable product standard and edition, customer specification, drawing revision, sampling plan, test methods, pass limits, marking text and certification responsibility. State whether the factory will use an existing approved design or develop a new product that needs qualification. Keep machinery acceptance separate from finished-product certification while connecting the same controlled drawing to both.
How to verify: Build a requirements matrix with one row for each cable characteristic and one column for the document, production control, test method, instrument and retained record. IEC 60228:2023 covers nominal conductor cross-sections, conductor constructions and resistance requirements for a broad range of power cables and cords, but the product-specific standard decides whether and how it applies.1 For PVC-insulated cable families within its scope, IEC 60227-1:2024 supplies general requirements and points to the relevant particular parts and test methods.2
Red flags: The quotation uses “IEC standard” without a number or edition, the supplier selects tests after the machine is built, or a proposed UL mark is treated as a machine feature rather than a finished-product certification responsibility.
3. Conductor Input: What conductor structure enters the insulation stage?
Why it matters: The insulation line sees a physical input, not a marketing name. Solid, stranded and fine-stranded conductors require different upstream preparation, reel formats, tension control and surface-condition checks. A factory that buys ready-to-insulate conductor needs a different project scope from a factory that begins with rod or individual fine wires.
What to ask: Define conductor material, solid or stranded construction, nominal size system, individual-wire data where applicable, compacted or non-compacted form, incoming package, allowable range, joint policy, surface condition and resistance acceptance. State whether drawing, annealing, tinning, bunching or rigid stranding is in the new project, already available in the factory or purchased as prepared conductor.
Cara memverifikasi: Periksa gambar konduktor yang telah disetujui dan satu reel masuk representatif. Hubungkan setiap transformasi yang diperlukan ke mesin dan pengukuran tertentu. Untuk proyek yang memerlukan proses drawing kawat tembaga antara, gunakan referensi mesin drawing kawat tingkat menengah untuk memeriksa ukuran inlet dan outlet yang diusulkan sebelum memilih peralatan hulu dan hilir. Konfirmasi paket pay-off, jalur panduan, rentang tegangan, dan antarmuka insulasi hilir terhadap konduktor aktual, lalu sertakan masukan yang sama dalam daftar material FAT. IEC 60228 terutama berkaitan dengan konduktor dalam kabel jadi, sehingga pembeli tetap memerlukan kontrol proses untuk konduktor antara yang memasuki produksi.1 Jika proyek mempertimbangkan persiapan konduktor secara internal, bandingkan permintaan bulanan dan anggaran yang tersedia dengan membeli konduktor yang sudah dipersiapkan. Dalam satu contoh proyek HONGKAI, permintaan yang hanya mencapai puluhan kilometer per bulan membuat pembelian konduktor siap pakai lebih praktis dibandingkan menambahkan peralatan drawing dan annealing yang tidak dapat dimanfaatkan penuh oleh pabrik; contoh tersebut bukanlah ambang batas universal, dan keputusan tetap bergantung pada komposisi produk aktual pembeli, kebutuhan bulanan, serta rencana investasinya.
Red flags: The supplier assumes copper when aluminum is possible, assumes a fine-stranded conductor can be handled like a solid conductor, or quotes a buncher without the individual-wire, finished-conductor and package definitions.
4. Conductor Forming: Does the route require bunching or stranding?
Why it matters: Bunching and ordered stranding are not interchangeable labels. The approved conductor construction, individual-wire input, finished size, lay requirements, package and downstream use decide the process. Flexible conductors commonly require a bunching stage, while other low-voltage power conductors may require a different stranding method; a solid conductor needs neither.
What to ask: Specify the individual-wire count and range, finished conductor construction, lay direction and required lay range, finished package, conductor test plan and intended insulation line. Ask whether the machine forms bare conductor, insulated cores or both, because those are different production tasks. Request a machine configuration tied to the exact input and output rather than to the largest model in a series.
How to verify: Run the agreed conductor using the specified pay-off and take-up packages, then verify the finished construction, dimensions, resistance and downstream handling by the project method. HONGKAI’s wire bunching machine reference shows that model selection changes with conductor input, finished size, lay range and package. The double-twist bunching machine reference is a separate equipment family and should be reviewed against the same approved conductor data.
Red flags: A proposal uses “stranding machine” without naming the process, quotes a maximum speed without the conductor and package, or cannot show how the finished conductor will feed the insulation stage.
5. Applied Layers: Which insulation and outer coverings must the line apply?
Why it matters: Material names alone do not define an extrusion process. The approved compound grade, conductor, layer construction, thickness controls, cooling route, marking method and finished handling determine the extruder, crosshead, tooling and auxiliary scope. THHN or THWN also should not be reduced to “ordinary PVC wire” because the designation and construction include specific marking and evaluation requirements.
Yang harus ditanyakan: Sediakan bahan isolasi dan selubung sesuai dengan grade yang disetujui, urutan lapisan, aturan ketebalan nominal dan minimum, rencana warna, persyaratan pemanasan awal konduktor jika ditentukan, hasil akhir permukaan, metode konsentrisitas, persyaratan uji percikan (spark-test), legenda cetak, batas pendinginan, dan kemasan jadi. Untuk konstruksi multilapis, identifikasi apakah lapisan-lapisan tersebut diaplikasikan secara tandem, diekstrusi bersama (co-extruded), atau diproduksi dalam proses terpisah sesuai proses yang telah disetujui. Untuk tinjauan konfigurasi HONGKAI THHN atau THWN, “PVC plus nilon” bukanlah informasi lengkap: struktur produk yang tepat, pencetakan yang dipersyaratkan, kemasan jadi, serta pengujian kabel yang dimaksudkan juga diperlukan agar perlengkapan aplikasi, penandaan, pengujian, dan penanganan dapat diselaraskan dengan cakupan ekstrusi.
How to verify: Review the cable cross-section and bill of materials with the tooling and auxiliary list. Challenge the proposal against every layer and require samples tied to the material lot, recipe, line condition and test results. The UL Solutions Wire and Cable Application Guide explains that THHN identifies thermoplastic insulation for dry use with a nylon jacket and that wire designations communicate intended use and evaluated characteristics.3 The buyer must still provide the exact product and certification basis for the target market.
Red flags: The machine list does not name how a nylon or other outer layer is applied, compound compatibility is assumed from a generic polymer name, or the supplier presents a cable designation as proof that the proposed line can meet it.
6. Core Assembly: Does the cable need cabling, shielding or an outer sheath?
Why it matters: An insulated single conductor can leave the extrusion stage as a finished product, but a flexible or control cable usually continues through additional assembly. Core count, lay, fillers, binders, identification, shield construction and outer sheath create new tension zones, pay-offs, tooling and acceptance checks. These stages must be mapped from the approved cable drawing rather than copied from a power-cable template.
What to ask: Define core count and identification, cabling lay, direction, filler and binder, shield material and coverage method when required, drain wire if specified, separator, inner covering and outer sheath. State which stages occur online and which are separate operations. Specify the reel presented by the insulation stage and the reel required by cabling or sheathing equipment.
Cara memverifikasi: Buat peta lapisan-ke-tahap dan telusuri jalur material dari inti berisolasi hingga kabel jadi. Periksa setiap posisi pay-off, antarmuka tegangan, panduan (guide), pengikat (binder), umpan perisai (shield feed), capstan, dan take-up terhadap gambar proyek. Perlakukan setiap lapisan yang ditampilkan sebagai masukan proses yang wajib: perisai yang dispesifikasikan memerlukan proses pelindungan yang sesuai, konduktor yang terbuat dari banyak kawat halus memerlukan proses bunching yang tepat, beberapa inti berisolasi memerlukan proses pengabelan (cabling), dan lapisan senyawa luar memerlukan proses pelapisan (sheathing). Oleh karena itu, konstruksi berselubung tunggal dan berselubung ganda tidak dapat diasumsikan menggunakan konfigurasi akhir yang sama. Rute tegangan rendah HONGKAI memperlakukan pelindungan dan perisai sebagai tahapan bersyarat; tahapan tersebut masuk ke dalam lingkup hanya jika desain kabel kontrol yang dikonfirmasi memerlukannya.
Red flags: The proposal assumes every control cable is shielded, uses one cabling arrangement for different core counts without review, or omits the reel and tension interface between core insulation and final assembly.
7. Testing and Handling: How will the factory prove and package the product?
Why it matters: A production route is incomplete if the factory can extrude cable but cannot measure, test, identify and package it as the approved product. Online checks support process control; routine and final tests support release. Coiling and reel handling also change with product dimensions, package rules, batch length and customer presentation.
What to ask: Define online diameter or other required gauges, spark testing where applicable, length measurement, print verification, conductor resistance, voltage or other product tests, sampling frequency, laboratory instruments, traceability fields, coil or reel format, standard length, wrapping, labeling and pallet requirements. State which instruments belong online, in a routine-test area or in the final laboratory.
Cara verifikasi: Lacak satu sampel FAT dari identitas bahan baku melalui resep, catatan online, hasil pengujian offline, dan label produk jadi. Bandingkan pencacah jalur dengan metode verifikasi panjang yang telah disetujui. Periksa kualitas koil atau gulungan pada kemasan target dan pastikan langkah penanganan berikutnya tidak merusak kabel atau mengaburkan ketertelusurannya. Susun FAT berdasarkan spesifikasi kabel target karena penggunaan peralatan bersama antar produk tetap bersifat spesifik konfigurasi. Pengujian rotasi tanpa beban bukan merupakan penerimaan produk jadi; catatan tersebut harus menghubungkan spesifikasi produk yang disetujui, konfigurasi mesin yang diuji, sampel yang diidentifikasi, dan hasil pengukuran.
Red flags: The quotation ends at the take-up, testing equipment is listed without methods or ranges, package requirements appear only after the FAT, or the sample label cannot be traced to its production and test records.
8. Factory Integration: Can every required stage operate as one controlled route?
Why it matters: Correct machines can still form a poor project if packages, line direction, utilities, floor space, control responsibilities and material flow do not connect. The production manager needs a route that operators can run, maintenance staff can access and quality staff can audit. Existing machines and planned expansion must be treated as real interfaces, not empty space on a layout.
What to ask: Provide the factory plan, usable floor area, access and lifting route, power and earthing data, cooling and compressed-air conditions, drainage, ventilation, raw-material storage, work-in-process path, laboratory location, existing equipment, maintenance clearance, staffing plan and expansion boundary. Request one responsibility matrix covering HONGKAI-manufactured equipment, specialist systems, buyer-supplied items and site work.
Cara verifikasi: Tinjau tata letak lengkap dan matriks utilitas sebelum konfigurasi dibekukan. Lacak pergerakan gulungan dari konduktor masuk hingga paket jadi dan catat setiap transfer manual. Tambahkan lembar antarmuka diameter dan paket yang mencatat diameter sebelum dan sesudah penggelembungan, jumlah inti, diameter sebelum dan sesudah ekstrusi, serta apakah setiap hasil tetap berada dalam rentang pemrosesan terverifikasi mesin yang dipilih. Pilih setiap take-up berdasarkan diameter kabel, ukuran gulungan yang diperlukan, dan rencana komersial, termasuk apakah pabrik menjual gulungan produksi secara langsung atau memindahkan kabel ke dalam kemasan penjualan yang lebih kecil. Pastikan akses perawatan, lorong operator, zona keselamatan, dan pengambilan sampel laboratorium tetap dapat digunakan selama produksi normal. Gunakan satu matriks FAT (Factory Acceptance Test) dan penerimaan di lokasi yang terhubung untuk antarmuka, alih-alih menerima demonstrasi mesin secara terpisah.
Red flags: The layout is created after ordering, auxiliary systems have no named supplier, packages change between stages without handling equipment, or utilities are described only as “standard factory supply.”
Note: A low-voltage cable production line becomes selectable only when every layer, transformation, interface and acceptance record can be traced back to the approved finished cable.
How Do Building Wire, THHN, Flexible and Control Cable Routes Differ?
Building wire, THHN or THWN, flexible cable and control cable should be treated as four reference routes rather than one universal line. Building wire may finish after conductor preparation, insulation, testing and coiling; THHN or THWN adds the layers and controls required by its approved construction. Flexible cable typically adds fine-wire bunching and may add cabling and sheathing, while control cable adds multicore assembly and only the shielding or protection shown in its design. HONGKAI maps each route from the finished-cable drawing and marks conditional stages separately.
| Reference cable | Preliminary production route | Buyer decision that changes the scope | Evidence to retain |
|---|---|---|---|
| Building wire | Prepared conductor → insulation → marking and testing → coiling or reeling | Solid, stranded or flexible conductor; insulation system; single pass or additional covering | Conductor record, material lot, dimensions, electrical test, print and package record |
| THHN / THWN | Approved conductor → thermoplastic insulation → nylon or approved outer layer → marking, testing and packaging | Exact designation, market standard, layer method, marking and certification responsibility | Controlled drawing, compound approvals, layer measurements, test and certification records |
| Flexible cable | Fine-wire preparation → bunching → core insulation → cabling when multicore → sheath when required → testing and handling | Strand construction, flexibility requirement, core count, cabling lay and sheath | Finished-conductor data, core identity, cabling and sheath records, final tests |
| Control cable | Conductor preparation → core insulation → multicore cabling → shielding or protection if specified → sheath → testing and handling | Core count, identification, shield construction, drain or binder, protection and installation environment | Core map, lay and shield evidence, sheath data, electrical tests and final label |
These routes are deliberately preliminary. A building wire made from prepared conductor may not need drawing or bunching in the new factory. A flexible single-core product may not need a cabling stage. A control cable without a shield should not receive shielding equipment merely because another control-cable design uses it.
The same discipline applies to machine-source claims. HONGKAI’s current low-voltage hub identifies selected core extrusion equipment as HONGKAI-manufactured and marks specialist machinery separately. The buyer should require that attribution in the technical offer, along with the interface owner, documents, FAT responsibility, spare-parts source and after-sales route for each supplied stage. HONGKAI’s cable machinery spare-parts page provides the identification path for replacement enquiries, but the project should still attach an initial parts list tied to the final equipment configuration.
Note: The product family narrows the process route, but the approved drawing decides which stages are mandatory, conditional or excluded.
What Evidence Should Be Written into the RFQ and FAT Plan?
The RFQ should describe the input, transformation, output and acceptance evidence for every required stage. The supplier should return a compliance matrix, equipment list, source attribution, interface schedule and FAT plan tied to the same cable drawing. HONGKAI machine references can support the preliminary configuration, but exact models, ranges, speeds, utilities and tests remain project-specific until the materials and product requirements are confirmed. A buyer should reject any value that cannot be traced to a stated operating condition and test method.
The following checklist turns the article into a procurement brief:
- ☐ Finished-cable drawing, designation, target market and controlled revision
- ☐ Product standard, customer specification, test methods and certification responsibility
- ☐ Conductor material, construction, size system, input package and acceptance data
- ☐ Gambar yang diperlukan, proses annealing, pelapisan timah, penggabungan atau pemintalan
- ☐ Bahan isolasi, pelindung, pelindung, pengikat, pengisi, dan selubung yang disetujui
- ☐ Urutan lapisan, dimensi, warna, tanda, dan persyaratan permukaan
- ☐ Jumlah inti, identifikasi, susunan pemasangan kabel, dan tahap perlindungan bersyarat
- ☐ Pemeriksaan online, uji rutin, uji akhir, pengambilan sampel, dan pelacakan
- ☐ Format gulungan atau reel, panjang standar, pembungkusan, label, dan persyaratan palet
- ☐ Mesin yang ada, arah jalur, transfer paket, dan batas ekspansi
- ☐ Tata letak, utilitas, antarmuka keselamatan, akses perawatan, dan staf
- ☐ Sumber peralatan, cakupan yang disediakan, eksklusi, dan tanggung jawab antarmuka
- ☐ Bahan FAT, kondisi operasi, aturan stabilisasi, sampel, dan kriteria lulus
- ☐ Manual, gambar, resep, pelatihan, suku cadang awal, dan serah terima dukungan
The RFQ should also distinguish a capability review from a guarantee. A supplier may show that a machine family can be configured for an input and output range, but the final proposal must identify the exact project condition. A maximum catalog speed does not prove stable production for the buyer’s conductor, compound, layer construction and package. Capacity should be balanced across every required stage and confirmed through agreed production evidence.
For a new factory, send the completed checklist and drawings through the HONGKAI project enquiry page. Untuk proyek ekspansi, tambahkan nameplate, manual, gambar gulungan, arah jalur, antarmuka kontrol, dan catatan produksi stabil dari peralatan yang ada. Bukti tersebut memungkinkan HONGKAI memisahkan cakupan penggantian, integrasi, dan peralatan baru tanpa mengasumsikan bahwa setiap aset yang ada kompatibel. Untuk pabrik baru dengan anggaran terbatas, tinjauan proyek oleh HONGKAI pertama-tama memetakan spesifikasi kabel yang didukung oleh pesanan saat ini. Keluarga kabel yang telah ditentukan dan direncanakan untuk kira-kira satu hingga dua tahun ke depan kemudian dapat ditinjau sebagai rute ekspansi, asalkan kompatibilitas tambahan tersebut tidak menambah biaya yang tidak proporsional dan tata letak awal tetap menyediakan ruang serta akses praktis bagi mesin-mesin masa depan yang telah dispesifikasikan.
Note: A strong quotation is not the longest equipment list; it is the shortest complete route whose inputs, outputs, interfaces and acceptance evidence match the cable the factory intends to sell.
-
IEC 60228:2023, Conductors of insulated cables. The official IEC page describes conductor cross-sections, constructions and resistance requirements and notes that product-specific standards decide applicability. ↩ ↩
-
IEC 60227-1:2024, Polyvinyl chloride insulated cables of rated voltages up to and including 450/750 V — Part 1. The official IEC page identifies the general scope and the particular parts and test methods needed for specific cable types. ↩
-
UL Panduan Aplikasi Kabel dan Kawat. Panduan resmi menjelaskan penamaan kabel, tanda-tanda, dan hubungan antara identitas produk, penggunaan yang dimaksud, dan bukti sertifikasi.↩
 English
 हिन्दी
 فارسی