
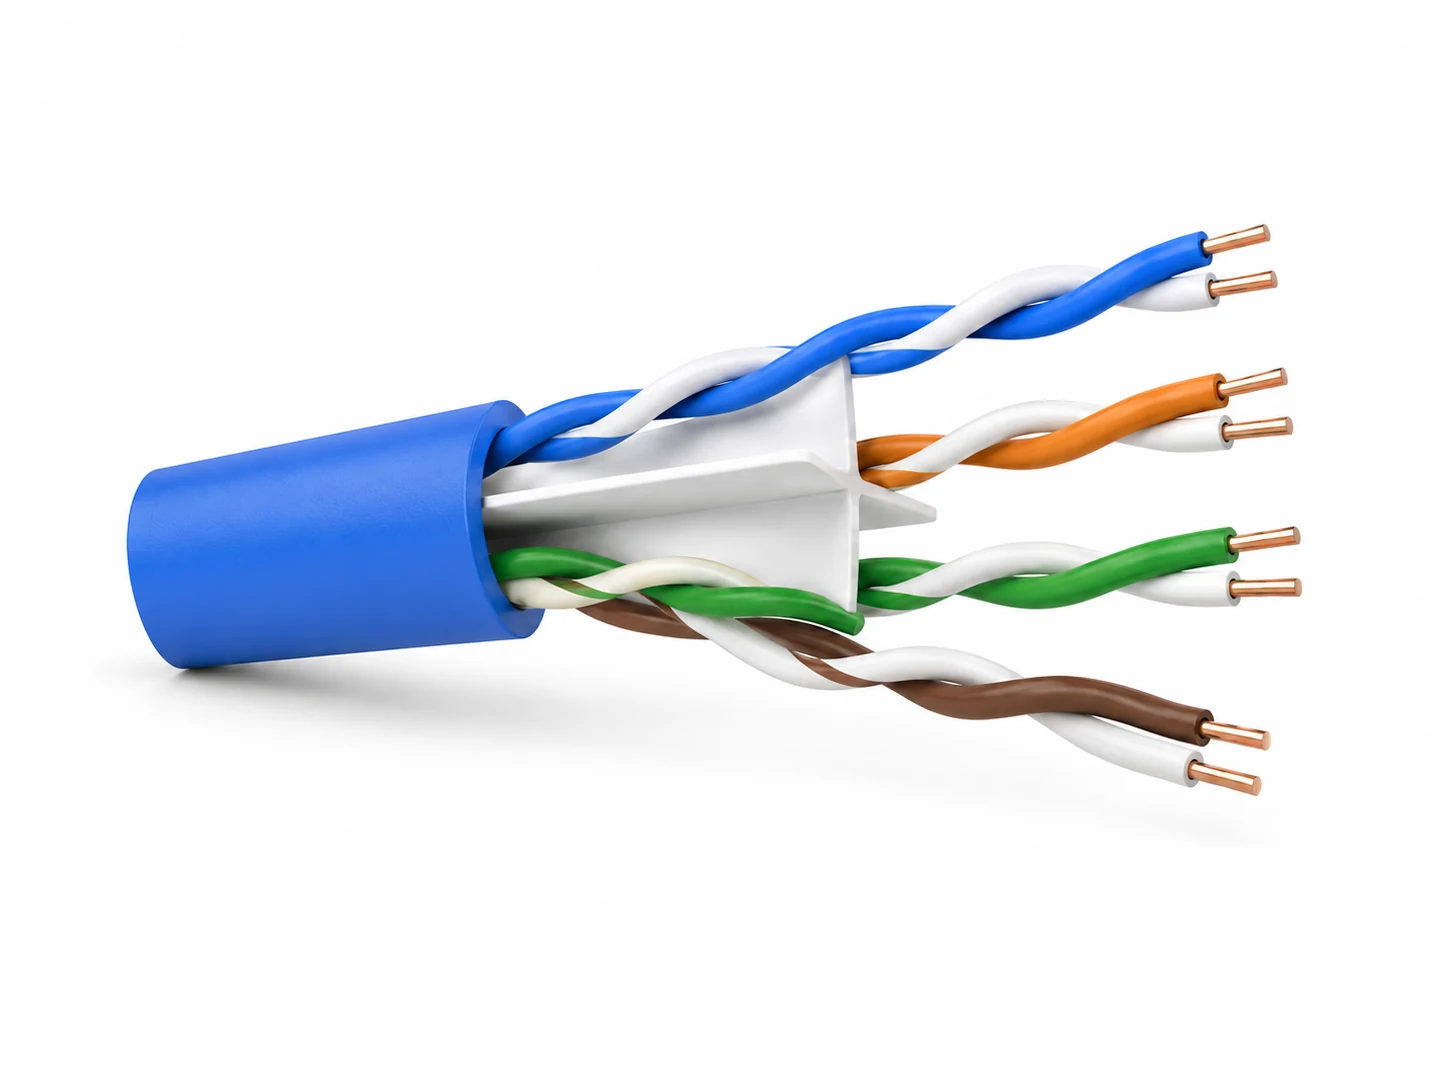


خط تولید لوله شل
Secondary coating · Manual & semi-automatic reel change
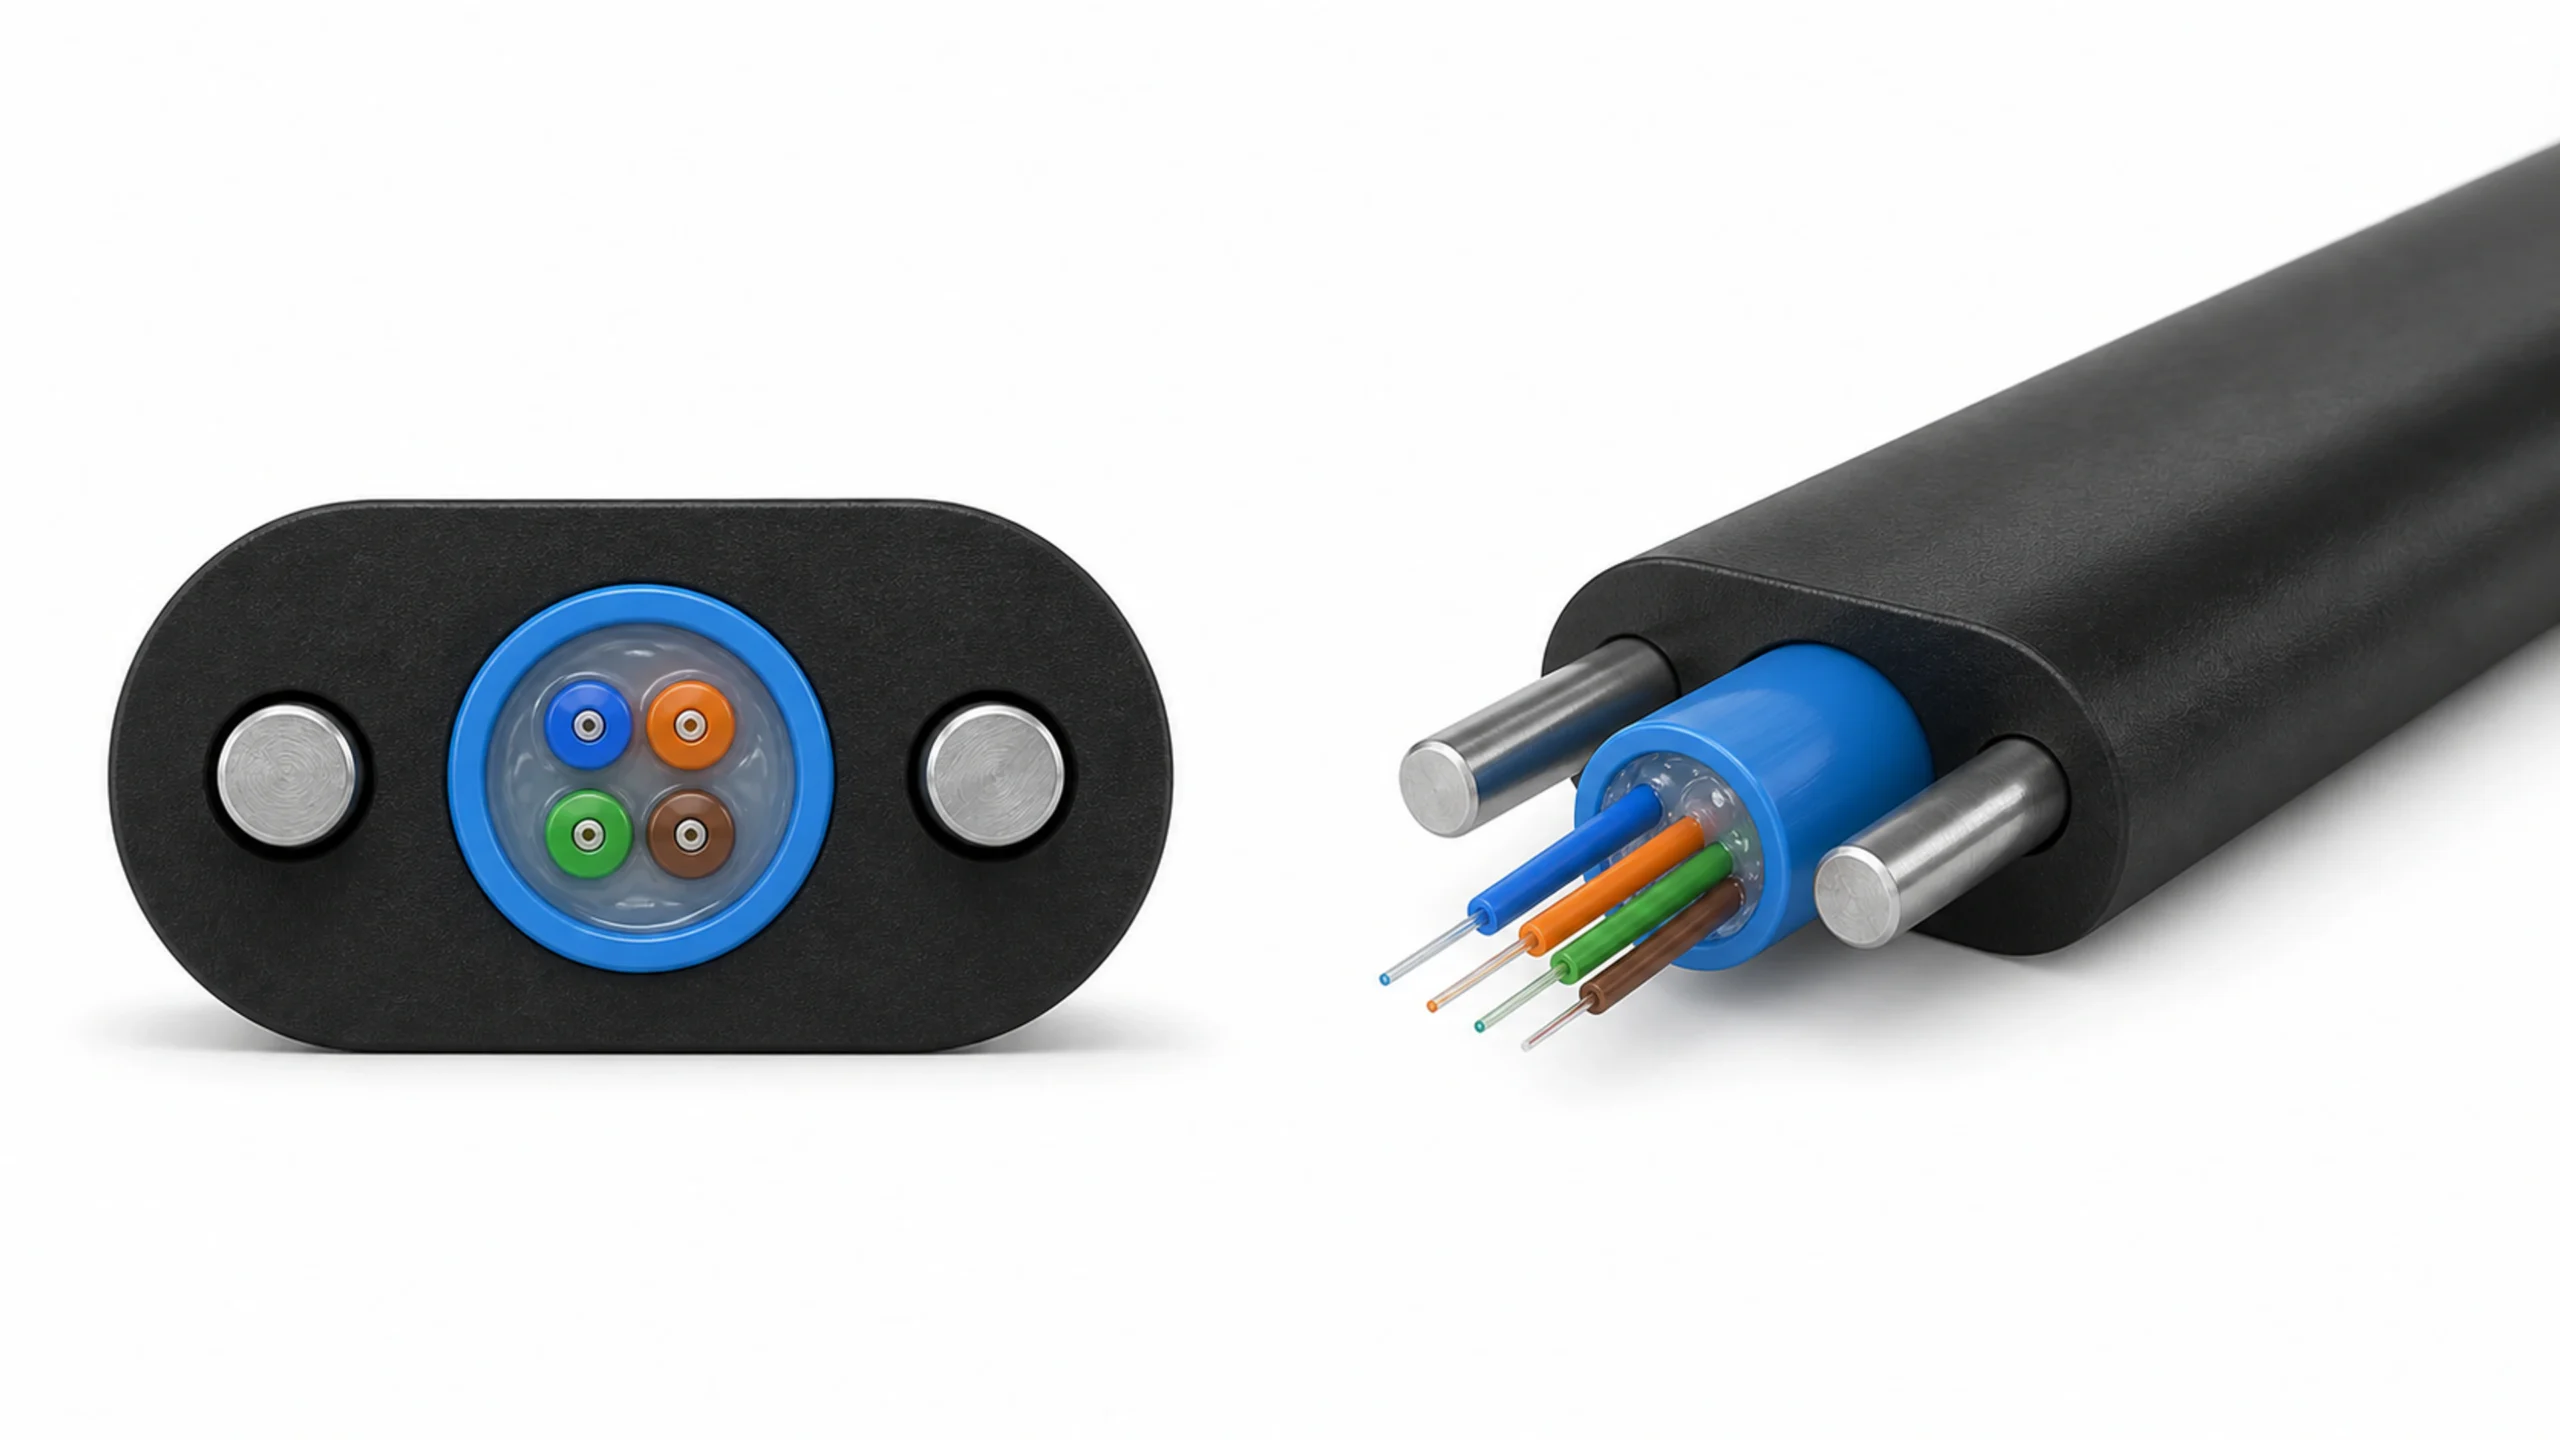
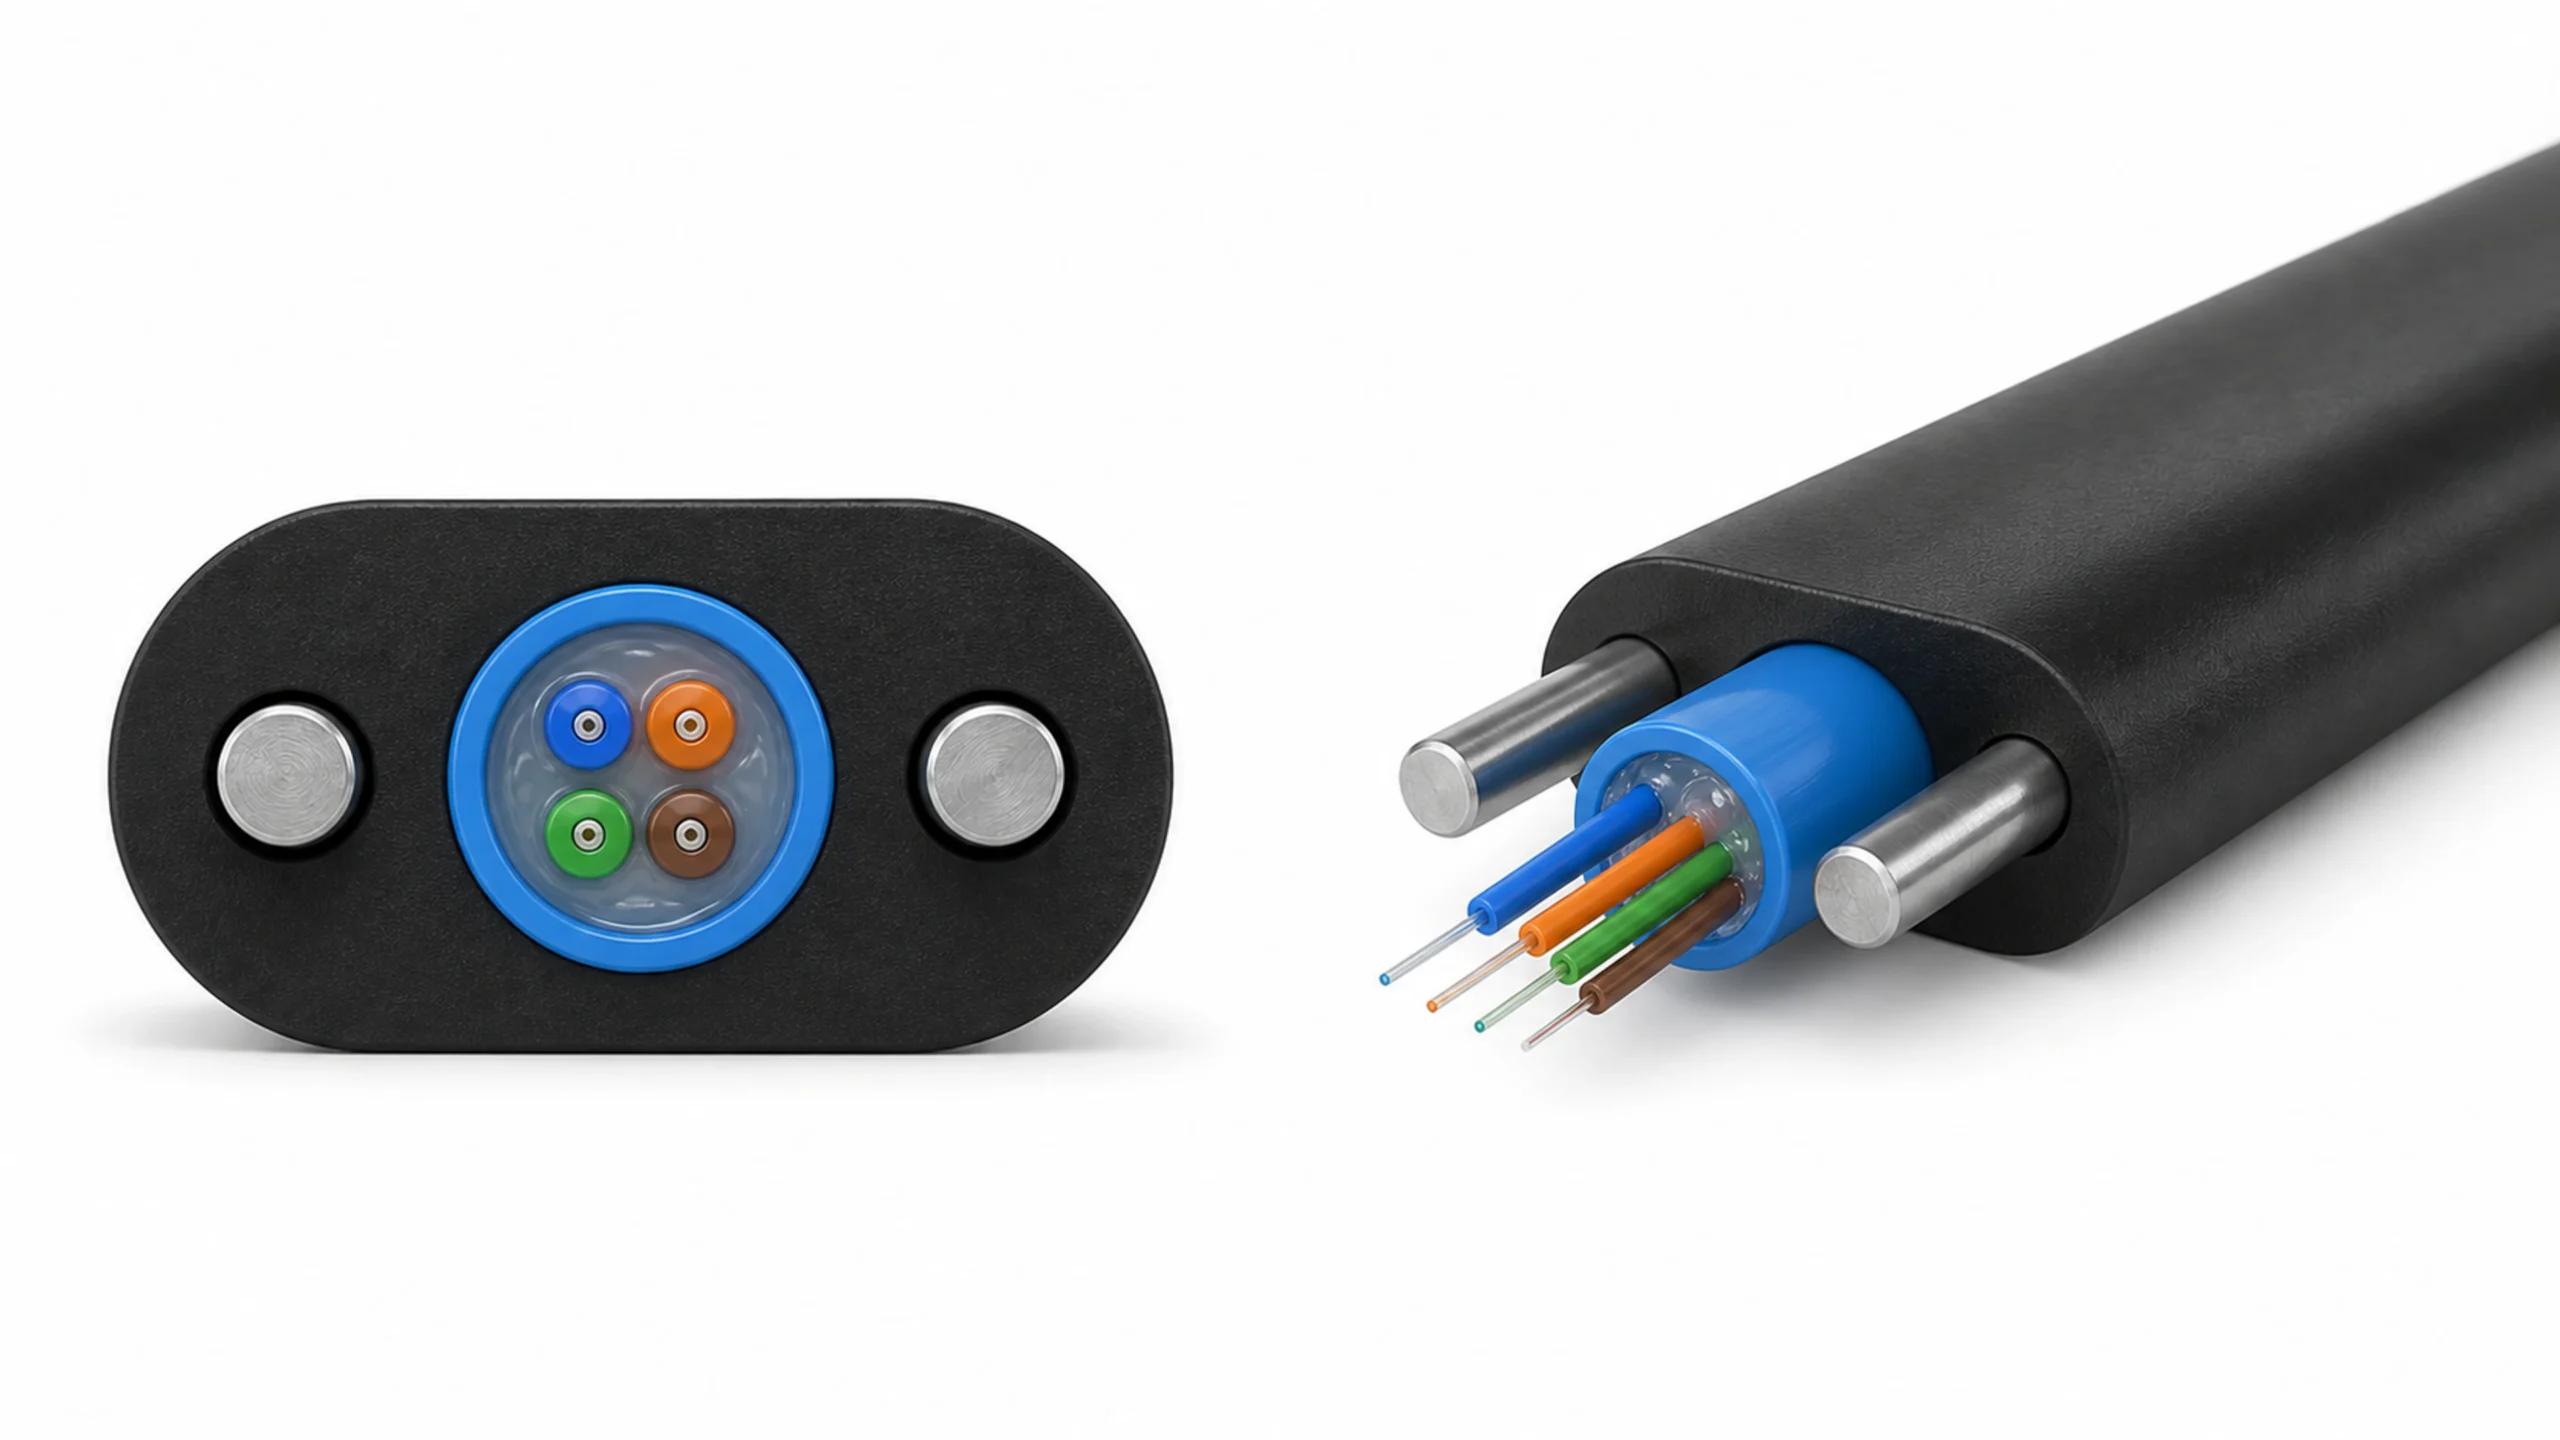
تولید المان لولهای شل مورد استفاده در کابلهای نوری مرکزی و کابلهای نوری با ساختار رشتهای. بررسی عملیات کار با فیبر، اکستروژن لوله، خنککاری و پیچش بهعنوان یک فرآیند هماهنگ، سپس مقایسه تعویض دستی قرقره با پیکربندیهای نیمهخودکار تعویض قرقره HK-50 a و HK-60.
- INPUT
- Approved fibers, tube polymer and specified filling system
- QUALIFIED OUTPUT
- Loose tube on the confirmed output package
- CORE PROCESS
- Pay off → apply specified filling / water blocking → extrude → cool → measure → take up
- APPLICATION
- Central-tube and stranded loose-tube cable routes
Scope boundary: this page covers secondary coating only. Fiber coloring, cable-core stranding, armoring and final sheathing remain separate stages unless included in a wider written proposal.
One process family. Four different reasons to configure it.
The equipment family is selected from the cable route, material path, output package and factory interface—not from a model number alone.
Form one qualified loose tube for an approved central loose-tube cable construction.
Confirm the tube construction, strength-member arrangement and downstream sheathing interface.
Prepare multiple loose tubes for the following SZ core-forming stage.
Confirm tube quantity, fillers, central member and the package handed to stranding.
Replace or extend one part of an operating secondary-coating line.
Document retained equipment, mechanical interfaces, signals, line direction and ownership.
Plan a complete loose-tube workshop around product and factory conditions.
Review materials, packages, utilities, layout, testing and operator workflow together.
Define the handoff before defining the machine.
The same visible line can represent different supply boundaries. The proposal should make each responsibility explicit.
Buyer provides
- Approved cable and loose-tube drawings
- Optical-fiber specification and supply package
- Tube polymer, masterbatch and filling requirements
- Target output reel or package
- طرح چیدمان کارخانه، تأسیسات و تجهیزات باقیمانده
- روش آزمون محصول و معیارهای پذیرش
HONGKAI configures
- ماژولهای تخلیه و جابجایی فیبر
- رابط پرکننده یا رابط مسدودکننده آب مشخصشده
- محدوده آمادهسازی مواد، اکستروژن و ابزارها
- خنککاری، اندازهگیری، کشش و همگامسازی
- Manual or semi-automatic reel-handling arrangement
- Reference layout, controls, interlocks and FAT plan
Jointly confirm
- Material and tooling compatibility
- Tube geometry and production window
- Excess-fiber-length control and test method
- Reel-change sequence and permitted interruption
- Inclusion, exclusion and downstream handoff
- FAT samples, acceptance evidence and services
Choose how the line handles the next reel.
Manual reel change uses the FTTH drop-cable-style dual-axis take-up. HK-50 and HK-60 share the same semi-automatic take-up. Compare operator tasks and equipment-assisted steps here, then review each complete line's extrusion, cooling and production requirements separately.
Explore the equipment behind each process.
Select a numbered marker or a module below to locate its equipment in the complete line and view the matching 3D detail. All equipment details open here, without leaving the page.

01 · Multi-position fiber pay-off racksLine entrance · the two fiber pay-off racks
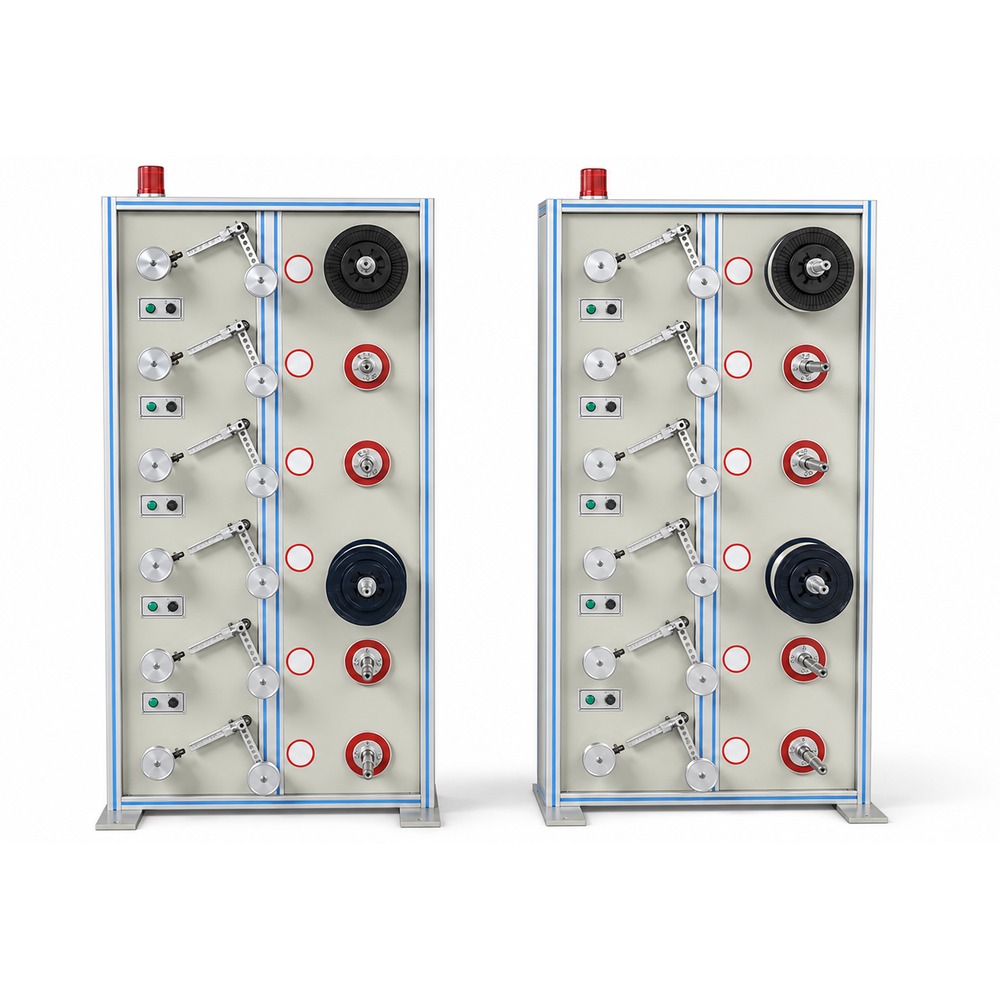
12-head pay-off assembly · proposal equipment reference, not the total line quantity
Multi-position fiber pay-off racks
The rack group at the line entrance feeds optical fibers toward extrusion. The detail shows the proposal's 12-head pay-off assembly; total rack quantity, package count, tension control and fiber routing follow the approved tube construction.
Confirm fiber count, input reel dimensions and tension requirements.
Selected module 01: Multi-position fiber pay-off racks. Line entrance · the two fiber pay-off racks.
Reference architecture: ten process responsibilities do not mean ten separate machines. Solid outlines locate visible equipment; the dashed outline marks an interface that is not separately resolved. Final hardware and layout follow the approved configuration.
Compare structure, operation and production requirements.
Use the same product and acceptance conditions to compare all three configurations. Rated speed, stable running speed and net production output are different values; request each with its stated trial conditions.
Swipe across the table to compare all three configurations.
| Review item | ManualOperator-managed change | HK-50 ReferenceSemi-automatic change reference | HK-60 ReferenceSemi-automatic change reference |
|---|---|---|---|
| Take-up arrangement | FTTH-style dual-axis take-up with operator-managed reel change | Shared semi-automatic take-up — same arrangement as HK-60 | Shared semi-automatic take-up — same arrangement as HK-50 |
| Changeover approach | Operator-managed reel replacement | Define operator tasks and assisted transfer steps for HK-50 | Define operator tasks and assisted transfer steps for HK-60 |
| Continuity & accumulation | Confirm whether a controlled stop is acceptable | Define storage, transfer and permitted interruption together | Size storage and transfer for the reviewed production requirement |
| Extrusion & cooling | از بین کشش لوله و ماده انتخاب کنید | Confirm the HK-50 screw, tooling and cooling configuration | Confirm the HK-60 screw, tooling and cooling configuration separately |
| سرعت خط و خروجی | Assess stable running plus reel-change and restart time | Quote running speed and net output for the specified product | Quote its own operating window; do not reuse HK-50 values |
| محدوده لوله و قرقره | Confirm tube OD, wall thickness, fiber count and output reel | محدوده لوله، ابعاد سیمپیچ و سازگاری انتقال را تأیید کنید | محدوده لوله، ابعاد سیمپیچ و سازگاری انتقال را تأیید کنید |
| Operator tasks | تعویض ردیف، راهاندازی مجدد و بررسیهای کیفی | Reel preparation, removal, replenishment and fault recovery | Reel preparation, removal, replenishment and fault recovery |
| Acceptance trial | توقف کنید، ردیف را تعویض کنید، دوباره راهاندازی کنید و کیفیت لوله را بررسی نمایید | Witness transfer, winding, alarms and tube quality at changeover | Witness the agreed HK-60 sequence with its own trial conditions |
Numerical specifications are not yet confirmed for these three configurations. Compare their separate technical proposals against the same tube drawing, materials, reel package and output target.
Open the detailed engineering checklist
Product & material
- Loose-tube drawingTO CONFIRM
- Fiber count & input packageTO CONFIRM
- Polymer and color systemTO CONFIRM
- Filling / water blockingTO CONFIRM
- Tooling scopeTO CONFIRM
کنترل فرآیند
- Pay-off tensionTO CONFIRM
- Extrusion monitoringTO CONFIRM
- Cooling zonesTO CONFIRM
- Online measurementTO CONFIRM
- EFL strategyTO CONFIRM
Reel handling
- Manual / semi-automaticTO CONFIRM
- AccumulationTO CONFIRM
- Transfer & cuttingTO CONFIRM
- Operator interventionTO CONFIRM
- Restart qualityTO CONFIRM
Factory integration
- Line directionTO CONFIRM
- Available footprintTO CONFIRM
- UtilitiesTO CONFIRM
- Retained equipmentTO CONFIRM
- Control signalsTO CONFIRM
Acceptance boundary
- Buyer materialsTO CONFIRM
- FAT productsTO CONFIRM
- Sampling methodTO CONFIRM
- Changeover trialTO CONFIRM
- Handover scopeTO CONFIRM
Match the equipment to your product mix.
Provide your tube drawing, expected output and reel-change requirement so that extrusion, cooling, accumulation, take-up and controls can be reviewed as one line.
One loose-tube stage. Multiple cable applications.
See where secondary coating fits into each complete cable-production route. Central-tube constructions proceed to their specified protection and sheathing stages; stranded constructions need a cable-core forming stage first.
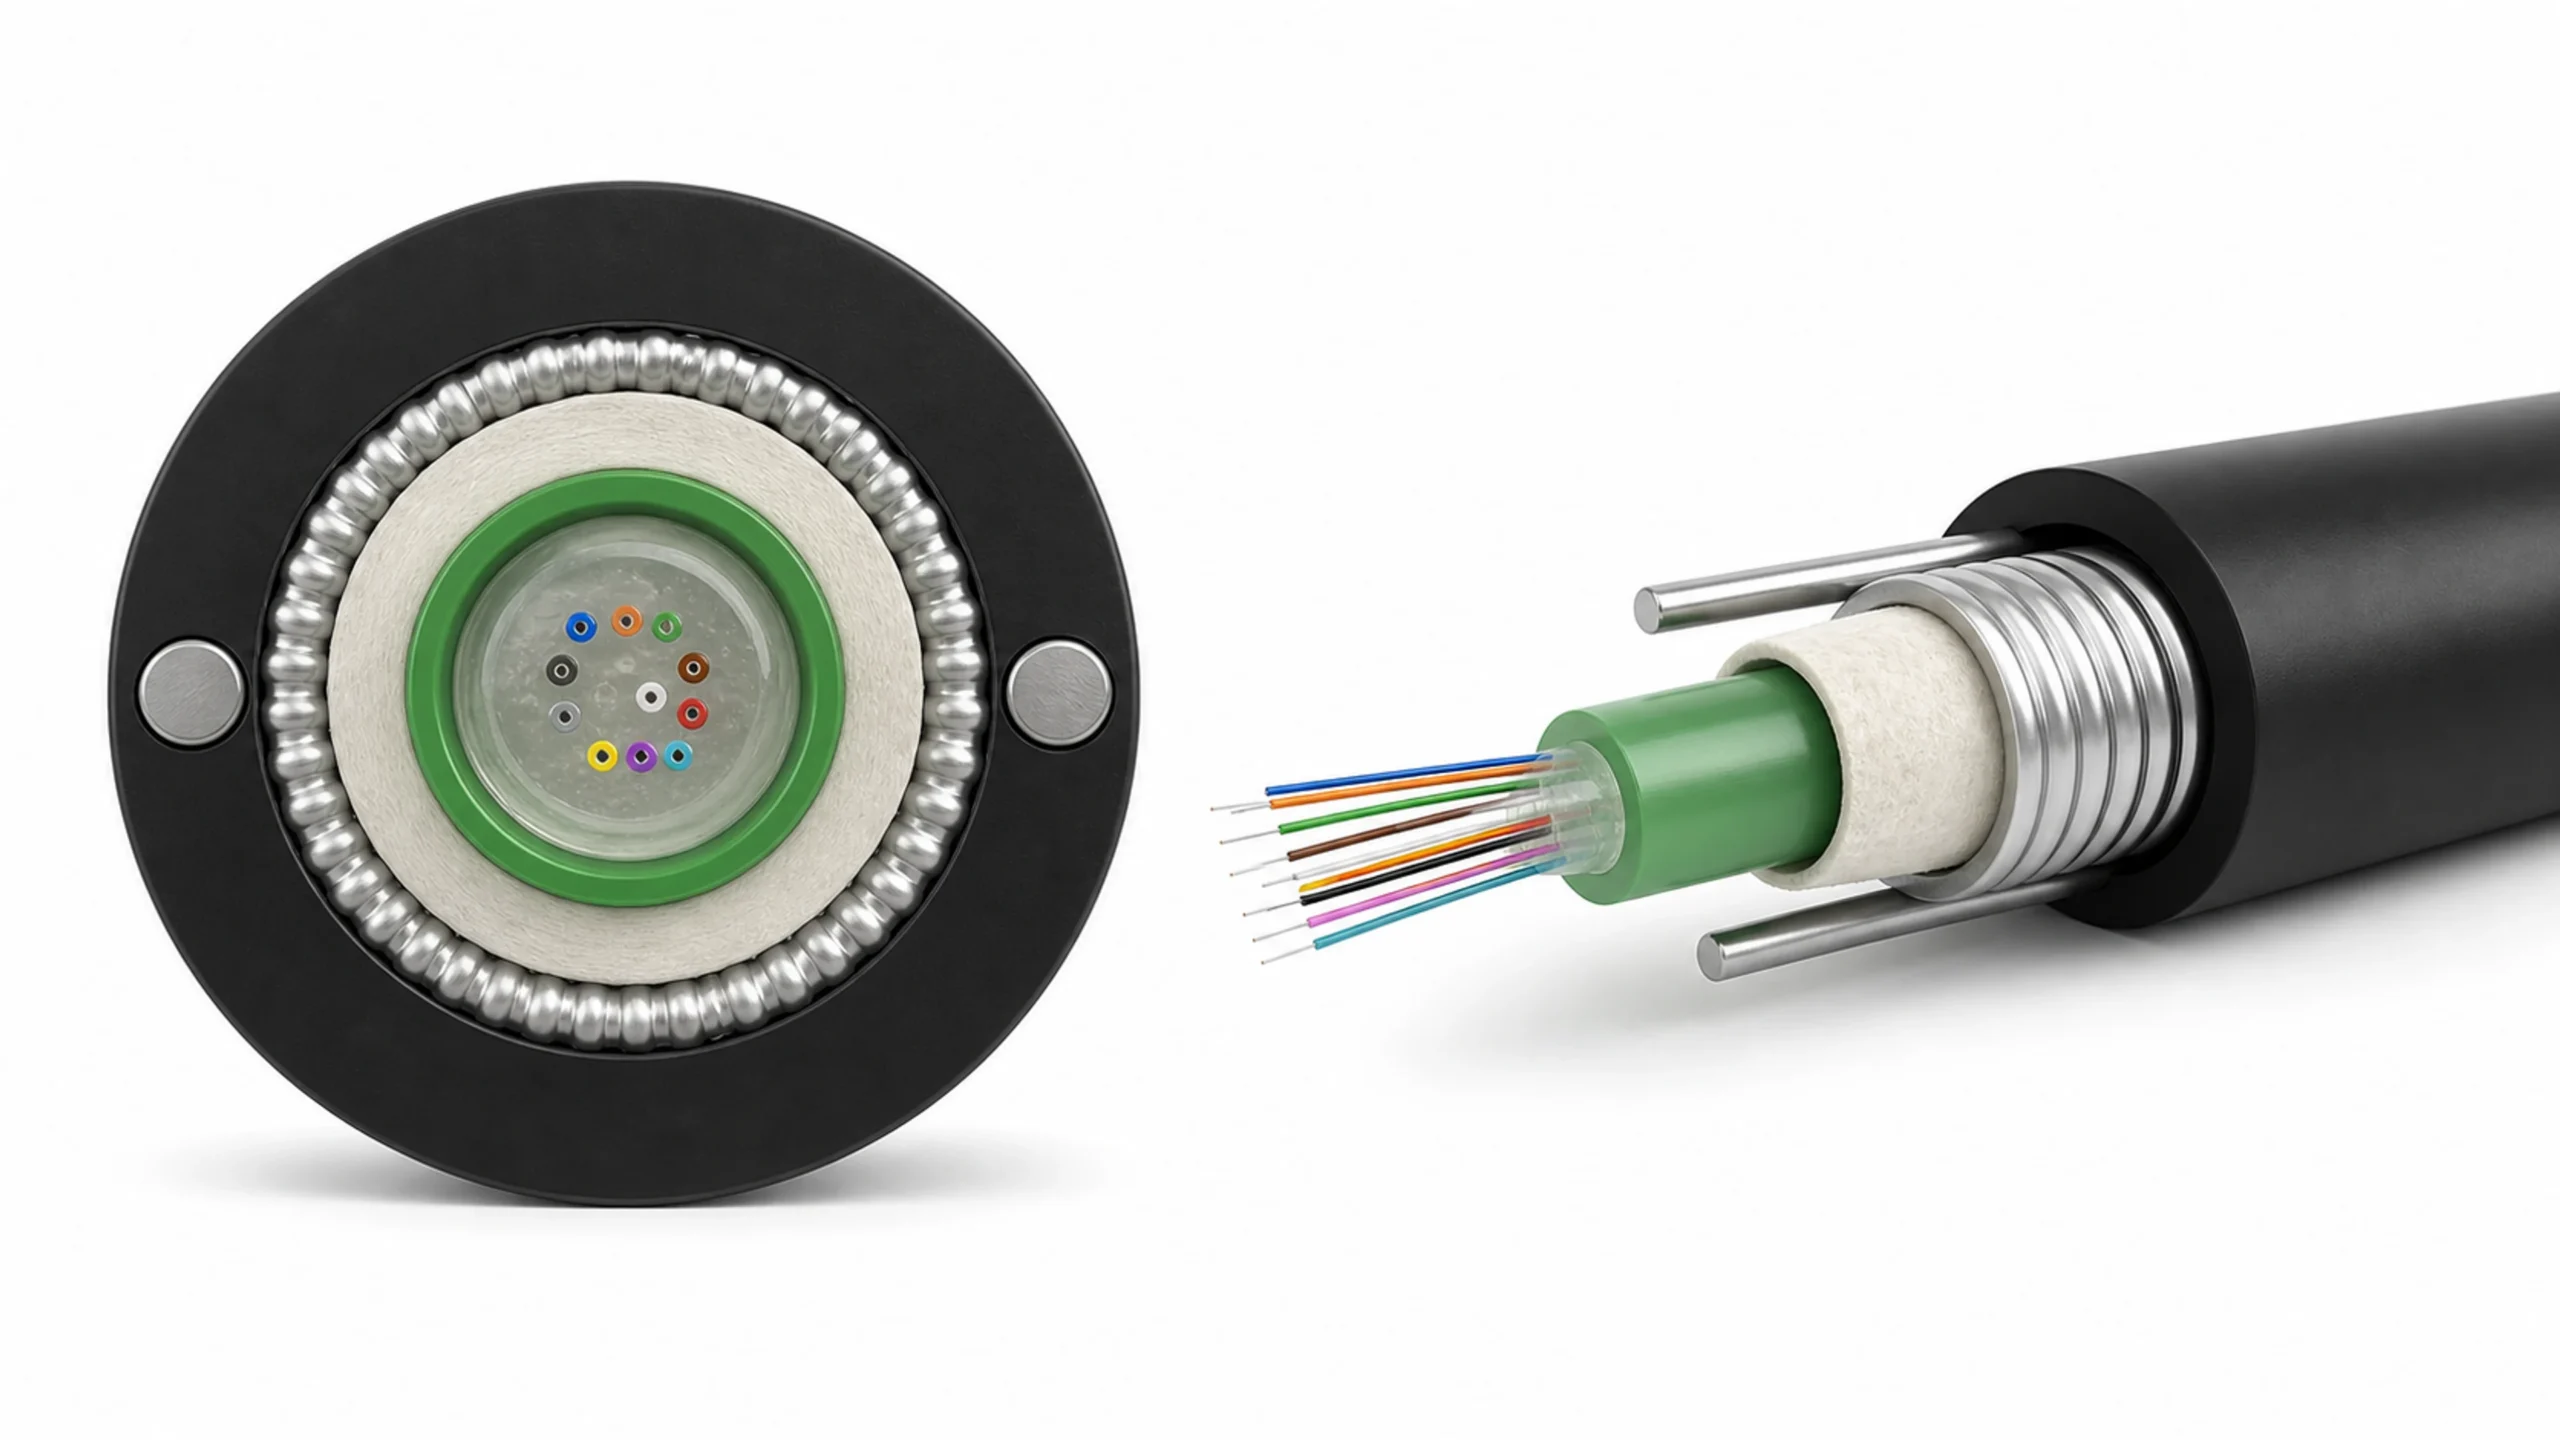
GYXTW Central Loose-Tube Cable
The process forms the central loose tube before the protection, armoring and sheathing stage.
Open cable solution
GYXTPY Small-Oval Central Loose-Tube Cable
The loose-tube element proceeds to parallel strength-member integration and final sheathing.
Open cable solution
Central Loose-Tube ASU Cable
The central PBT loose tube feeds the approved non-metallic forming and sheathing route.
Open cable solution
Stranded Loose-Tube Micro Cable
Individual loose tubes proceed to compact SZ cable-core formation before final PE sheathing.
Open cable solution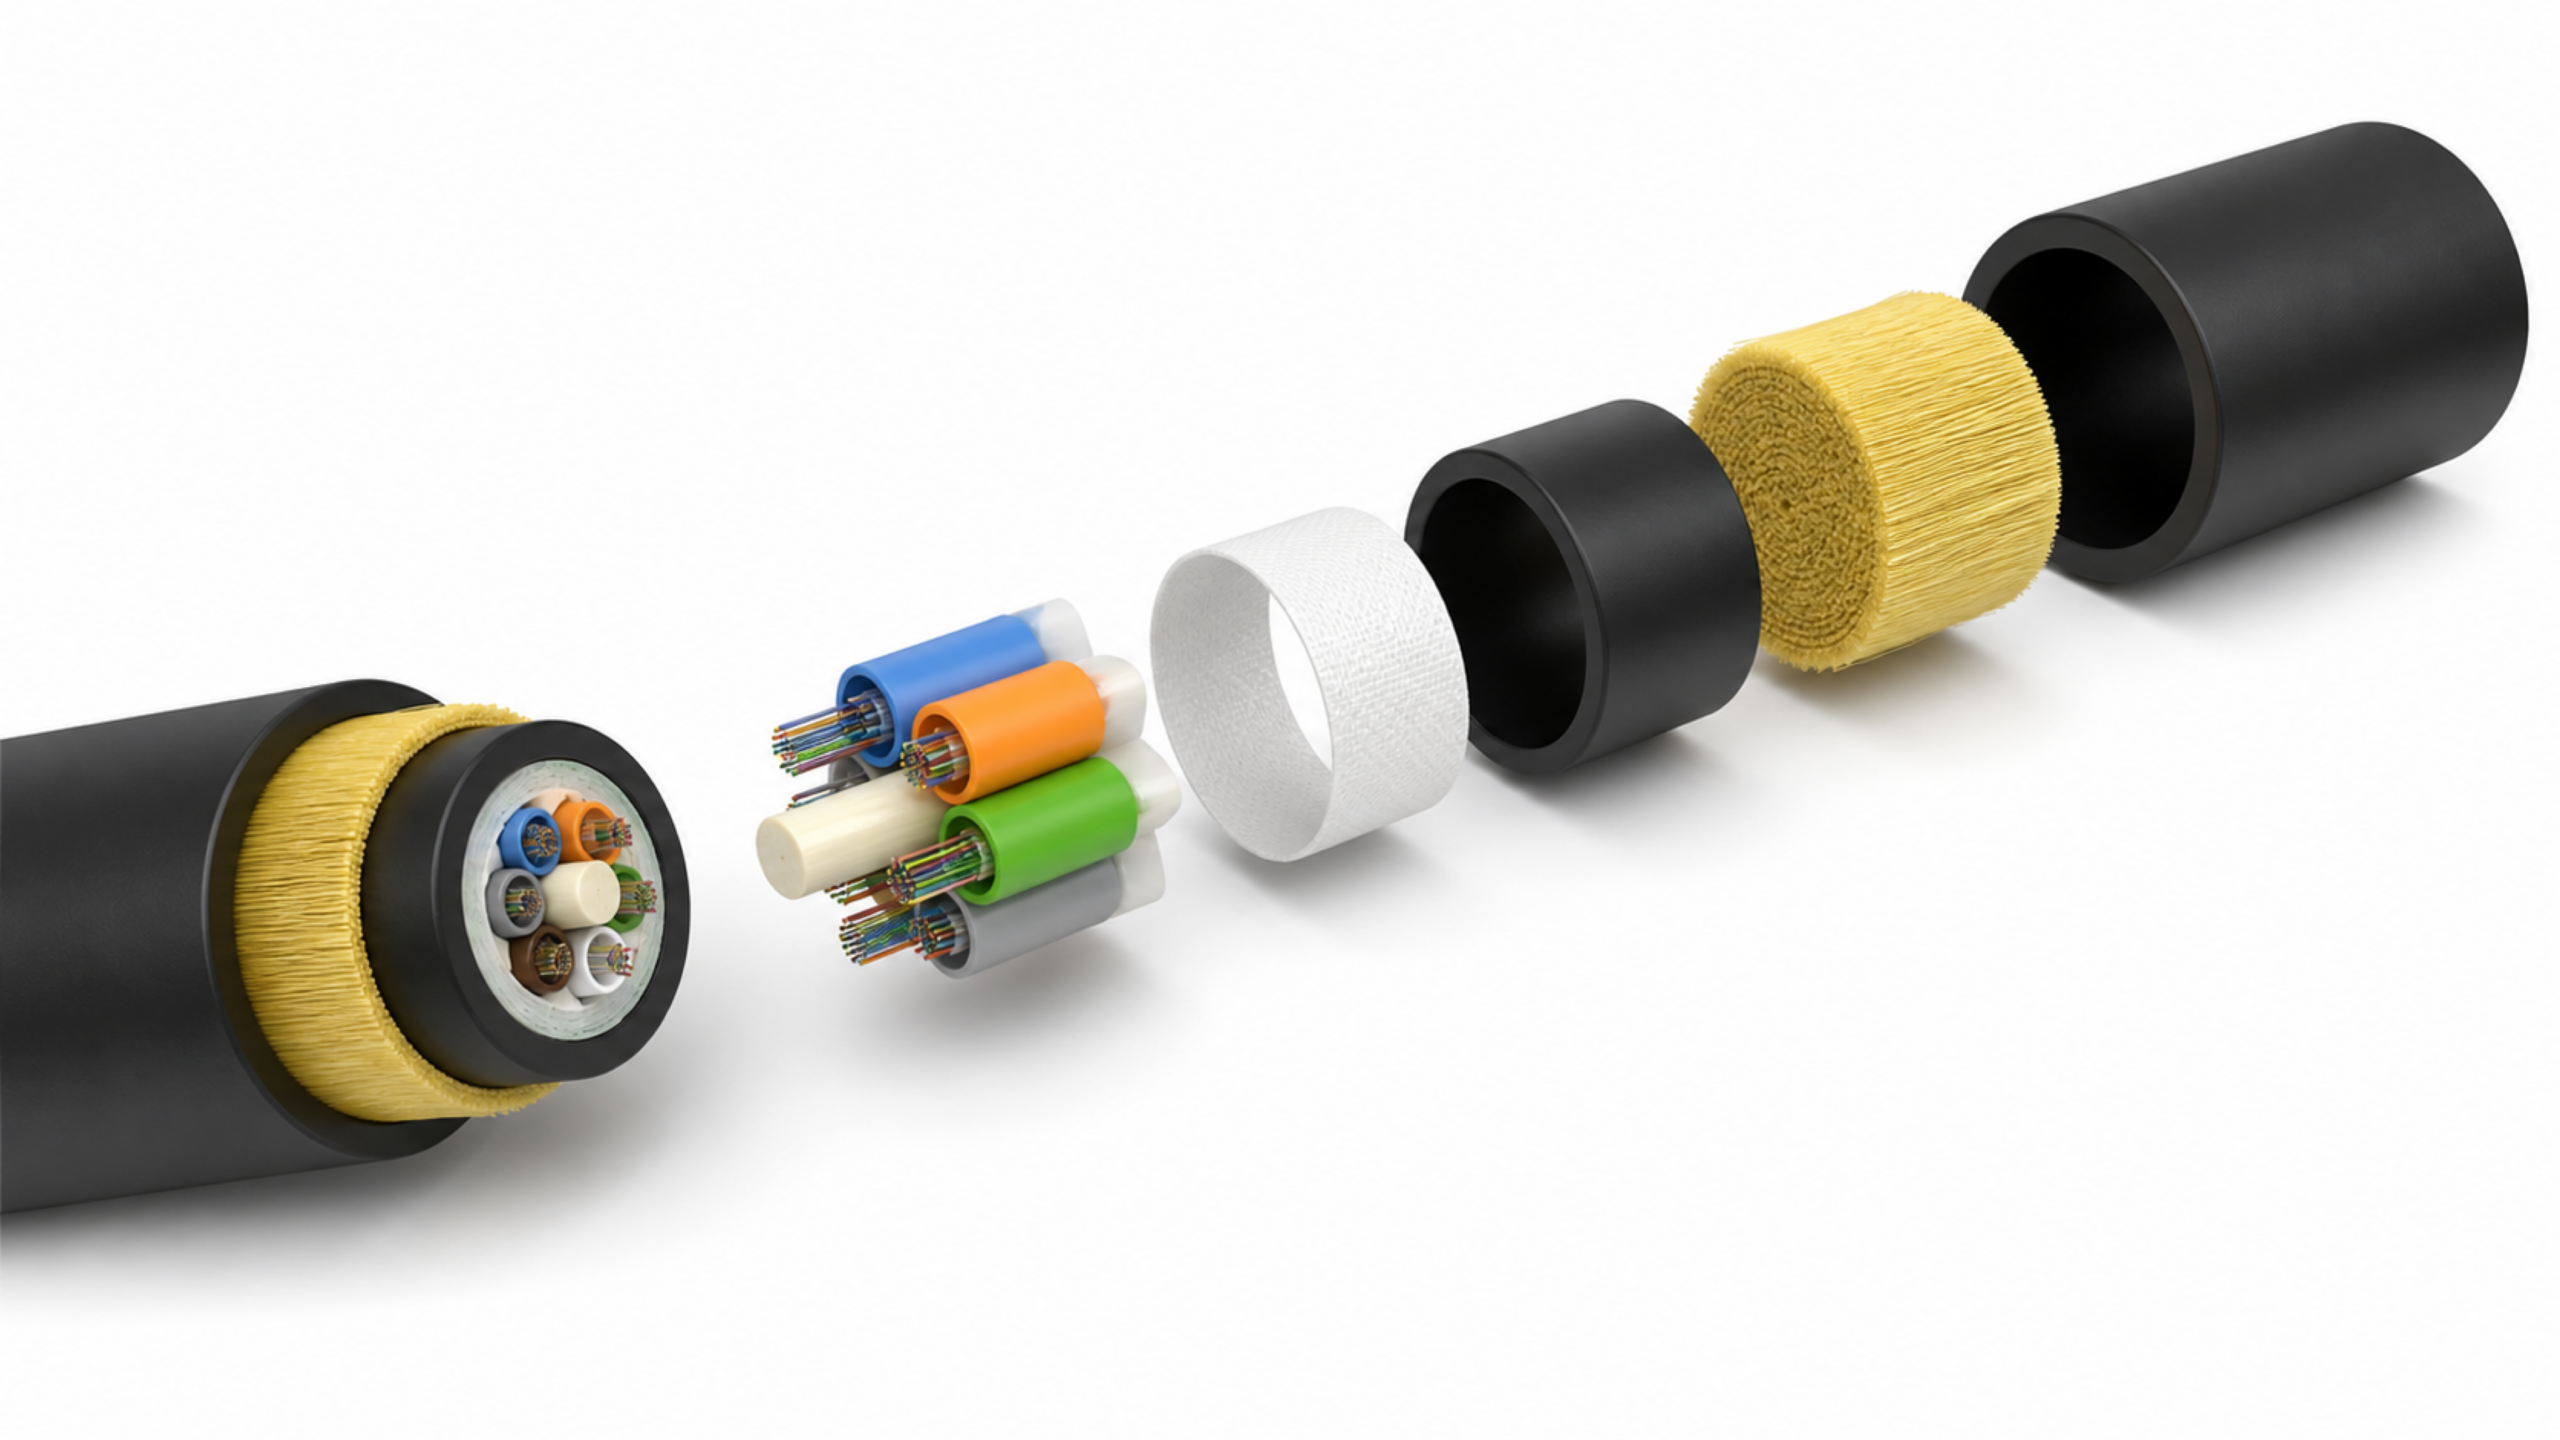
Stranded Loose-Tube ADSS Cable
Loose tubes feed SZ stranding, all-dielectric reinforcement and final sheathing.
Open cable solution
GYXTC8S Figure-8 Cable
The referenced loose tubes proceed to SZ core formation before GYXTC8S armoring, messenger positioning and figure-8 sheathing.
Open cable solutionFunction before model code: these cards refer only to the published cable constructions on their linked solution pages. Other central-tube or stranded loose-tube constructions require drawing review. FTTH drop, tight-buffered, GJFJV, GJFV and Patch Cord routes are not included merely because another page may use an HK-50 label.
Use the visual to plan the proof—not to replace it.
3D models support configuration review. The approved FAT plan establishes what the project must actually demonstrate.
Visible equipment arrangement
Use the 3D model to discuss module order, material path and the arrangement being reviewed.
Final values or acceptance
It does not confirm final quantity, footprint, speed, capacity, continuity or an accepted result.
The agreed operating boundary
Verify product, materials, controls, alarms, reel-change sequence, waste and restart quality.
Real project records. Loose-tube priorities made specific.
These HONGKAI-authored summaries connect existing customer project records with the equipment and engineering responsibilities reviewed for a loose-tube production line. They are not presented as verbatim quotations or customer-issued ratings.

Equipment review
- تجهیزات
- Fiber handling, the filling-system interface, extrusion, staged cooling, online measurement and reel handling were reviewed as one connected loose-tube process.
- HONGKAI support
- HONGKAI organized the discussion around the approved tube construction and the downstream cable-production route.

Engineering coordination
- تجهیزات
- Tube polymer, filling method, tooling, cooling path, EFL control and the output package were treated as connected configuration inputs.
- HONGKAI support
- HONGKAI translated the available project information into an equipment scope and FAT checklist for technical review.

Project support
- تجهیزات
- Line interfaces, utilities, layout, controls, reel-change operation and acceptance samples were considered with the production equipment.
- HONGKAI support
- HONGKAI kept inclusions, exclusions, handoff responsibilities and the acceptance boundary visible throughout project planning.
Source boundary: names, roles and photos follow existing HONGKAI customer records. The loose-tube-specific wording is prepared by HONGKAI from project-review priorities; no star score, verbatim endorsement, Review or AggregateRating markup is asserted.
Tell us what you need to produce or improve.
Share your project and contact details. Add specifications or drawings if available; unknown technical values can be confirmed during the engineering review.
Nine inputs make the first review useful.
- 01
Target cable family and loose-tube drawing
- 02
Fiber count, specification and supply package
- 03
Tube polymer, masterbatch and filling system
- 04
Manual or semi-automatic reel-change preference
- 05
Output reel dimensions and planned batch length
- 06
Whether a controlled stop is acceptable
- 07
Existing upstream and downstream equipment
- 08
Factory layout, utilities and line direction
- 09
Required FAT products and acceptance method
Questions before you specify the line.
Review cable compatibility, reel-change operation and the information needed for a project-specific proposal.
01آیا HK-50 a و HK-60 از سیستمهای نیمهاتوماتیک جمعکننده متفاوتی استفاده میکنند؟
خیر. هر دو از همان چیدمان نیمهاتوماتیک پیچش که در اینجا نشان داده شده است، استفاده میکنند. تعویض دستی بوبین بهجای آن از سیستم پیچش دو محوره سبک کابل انشعابی FTTH استفاده میکند. استفاده مشترک از سیستم پیچش نیمهاتوماتیک باعث یکسان بودن کامل دو خط تولید نمیشود: فرآیندهای اکستروژن، خنککاری، سیستمهای کنترل و مقادیر تولید برای هر پروژه بهطور جداگانه بررسی میشوند.
02آیا این صفحه یک مشخصهٔ ثابت HK-50 است؟
خیر. این صفحهٔ مشترک خانوادهٔ فرآیند، یک مرجع تعویض دستی کلاف را با مراجع پروژهٔ HK-50 a و HK-60 مقایسه میکند که محدودهٔ تعویض نیمهخودکار کلاف آنها همچنان در حال بررسی مهندسی است. مقادیر نهایی اکسترودر، سیستم کنترل، بستهبندیها، فوتپرینت و پذیرش در پیکربندی کتبی پروژه تعریف شدهاند.
03آیا HK-60 a بهطور خودکار به معنای سرعت بالاتری نسبت به HK-50 است؟
خیر. تنها نام خانوادگی، سرعت، ظرفیت یا محدوده کلاف را اثبات نمیکند. این مقادیر مستلزم نقشه لوله تأییدشده، سیستم مواد، فهرست کامل تجهیزات و پیشنهاد فنی امضاشده هستند.
04کدام کابلهای نوری میتوانند از این فرآیند لوله شل استفاده کنند؟
راهحلهای پیوندخوردهٔ GYXTW، GYXTPY و ASU با لولهٔ مرکزی از یک عنصر لولهٔ شل مرکزی استفاده میکنند. راهحلهای کابل میکرو، ADSS و GYXTC8S مرجعشده از لولههای شل قبل از رشتهبندی هستهٔ کابل بهره میبرند. سازگاری همچنان به ساخت تأییدشده، جنس لوله، ابعاد و رابطهای پاییندست بستگی دارد. مسیرهای بافر محکمشده و کابل انشعابی فرآیندهای متفاوتی هستند.
05آیا خط میتواند به تجهیزات نگهداریشده متصل شود؟
بهصورت بالقوه. HONGKAI باید ابتدا رابطهای مکانیکی، سیگنالها، ابعاد بستهبندی، جهت خط، مسئولیتهای ایمنی و توالی عملیات را بررسی کند.
06FAT تعویض نیمهخودکار کلاف چه چیزی را باید نشان دهد؟
از محصول و مواد توافقشده باید برای شاهد بودن در موارد تجمع، انتقال، برش، مداخله اپراتور، هشدارها، وقفههای مجاز، ضایعات تعویض و کنترلهای کیفیت پس از راهاندازی مجدد استفاده شود.


