Loose-tube cable cores · Pay-off to finished core take-up
USD 101,800 per set
Quoted configuration: HK-800/12 PLC+IPC Control SZ Stranding Production Line. Ex-factory delivery; the buyer arranges and pays transport. Final equipment and tooling follow the agreed configuration schedule.
Bring loose tubes and the specified central member together in a controlled SZ-stranded core. Match tube handling, reversal, binding and water blocking to the cable drawing, then coordinate traction and take-up for the next production stage.
Review the stranding head together with tube tension, line speed and binding.
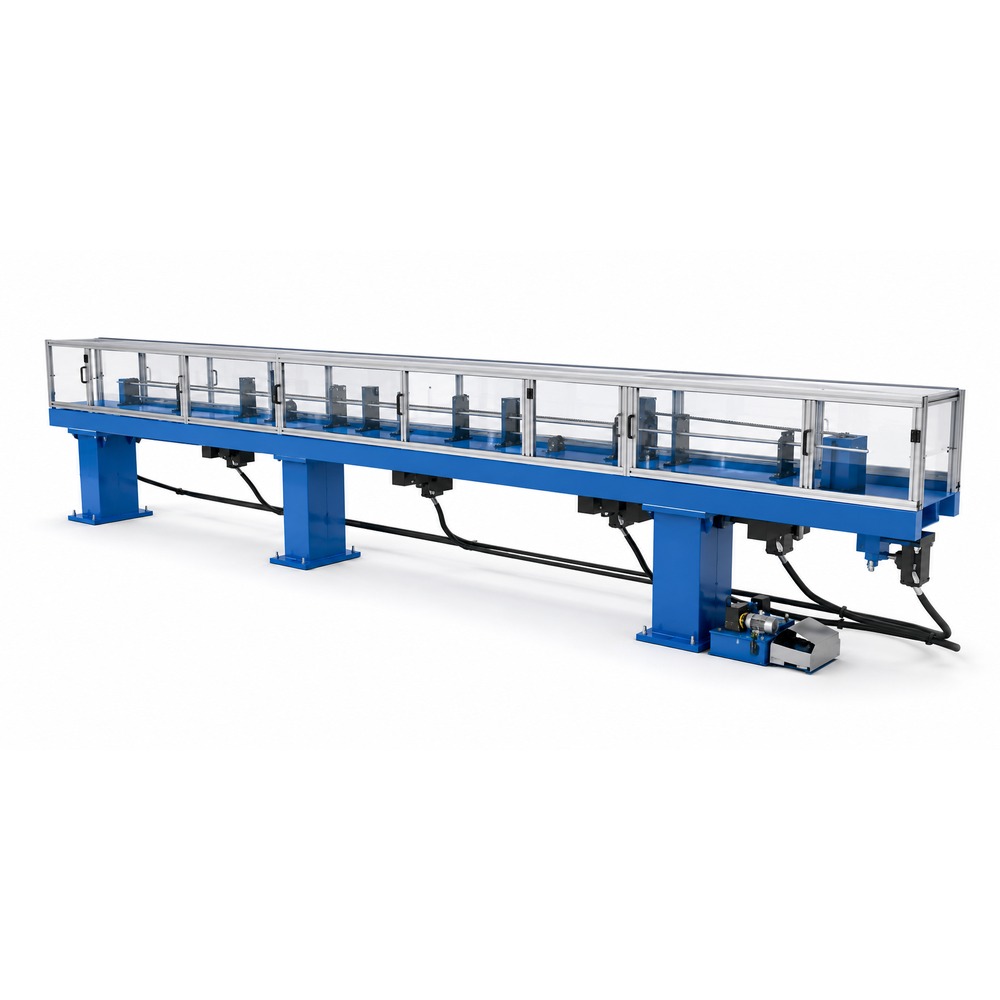
REFERENCE ARRANGEMENTEquipment quantities and final layout follow the reviewed project.
Scope boundary: this line forms the cable core. Loose-tube extrusion, final armoring, aramid reinforcement and jacket extrusion are separate stages unless specifically included in the written scope.
02PROCESS & MATERIAL HANDOFF
From separate loose tubes to one coordinated cable core.
Define the material entering and leaving the line before choosing machine quantities or a reference model.
01MATERIAL HANDOFF
Start with qualified tubes.
Confirm tube dimensions, identification, supply reels, the central member and any fillers before laying out the pay-off area.
02CORE FORMATION
Coordinate reversal and tension.
Review the SZ lay, reversal sequence and binding requirements against the approved cable-core drawing.
03CORE PROTECTION
Apply the specified package.
Filling compound, binding yarn and water-blocking tape depend on the construction. They are not interchangeable default packages.
04DOWNSTREAM HANDOFF
Deliver a core ready for the next stage.
കോർ നിശ്ചിത ഷീത്തിംഗ് അല്ലെങ്കിൽ സംരക്ഷണ ഘട്ടത്തിലേക്ക് പോകുന്നതിന് മുമ്പ് കോർ ജ്യാമിതി, റീൽ ബിൽഡ്, ഐഡന്റിഫിക്കേഷൻ, പരിശോധനകൾ എന്നിവ സ്ഥിരീകരിക്കുക.
03CONFIGURATION & PROJECT SCOPE
Configure the line around the core you need to make.
Start with the supply boundary and product mix. Model labels do not replace a review of tube handling, stranding, binding, traction and take-up.
CONFIGURATION BASISReference equipment · not three fixed machine packages
04EQUIPMENT IN THE LINE
Locate the machine. See its role in the core.
Select a marker or equipment card to highlight the corresponding area and open its image here. The complete line remains visible; the detail view preserves the original image proportions.
COMPLETE SZ PROCESS TRAIN · REFERENCE ARRANGEMENT
05 · SZ oscillatorHighlighted location in the reference process train
SELECTED EQUIPMENT · PROJECT REFERENCE05 / 12
Equipment arrangement for reference; the final configuration follows your approved technical proposal.
EQUIPMENT IN THIS LINE
SZ oscillator
Alternates the stranding direction to form the prescribed SZ lay around the central member. Coordinate reversal with incoming tube tension, traction and the downstream binding system.
CONFIRM FOR YOUR PROJECT
Tube paths, required pitch, reversal sequence, oscillator movement, line speed and core quality checks.
Selected equipment 05: SZ oscillator
Reference boundary: the panorama illustrates equipment order, not the final machine count, footprint or construction. Images from the project document show equipment families; the approved layout and equipment list define the supplied arrangement.
05TECHNICAL CONFIGURATION REVIEW
Compare the complete operating requirement—not one headline speed.
ലൈന് റിവ്യൂ ചെയ്യുമ്പോള് ഒരു നിശ്ചിത കേബിള്, മെറ്റീരിയല് പാക്കേജ്, ടെസ്റ്റ് രീതി എന്നിവ ഉപയോഗിക്കുക. ഘടകങ്ങളുടെ പരിധികളും ശുദ്ധ ഉത്പാദന ഔട്ട്പുട്ടും ഒരേ സംഖ്യയല്ല.
Inputs that determine the SZ line configuration
Review area
What to specify
Why it changes the line
Tube and package range
ട്യൂബ് വ്യാസം, ട്യൂബ് അളവ്, സപ്ലൈ റീലുകൾ, ഫില്ലർ ഘടകങ്ങൾ, സെൻട്രൽ-മെമ്പർ പാക്കേജ്.
Determine the pay-off arrangement and material path.
Core geometry
കോർ വ്യാസം, ലേ, റിവേഴ്സൽ പോയിന്റുകൾ, ബൈൻഡിംഗ് പിച്ച്, ടേക്ക്-അപ്പിന് ശേഷമുള്ള ജ്യാമിതി.
പൂർത്തിയാക്കിയ കോറിനെയും അതിന്റെ ഡൗൺസ്ട്രീം ഫിറ്റിനെയും നിർവചിക്കുക.
ജലത്തടയൽ സിസ്റ്റം
സംയുക്തം, വരണ്ട മെറ്റീരിയലുകൾ, ടേപ്പ് / നൂൽ ഫോർമാറ്റ്, അപ്ലിക്കേഷൻ സ്ഥാനങ്ങൾ, ക്ലീനിംഗ്.
കേബിൾ രൂപകൽപ്പനയ്ക്ക് അനുയോജ്യമായ മെറ്റീരിയൽ പാക്കേജ് തിരഞ്ഞെടുക്കുക.
Speed and synchronization
നിശ്ചിത കേബിളിനായി ആവശ്യമായ സ്ഥിരമായ വേഗത, സ്റ്റാർട്ട്/സ്റ്റോപ്പ് പെരുമാറ്റം, കൂടാതെ ചേഞ്ചോവർ നഷ്ടം.
Review the complete line, not one motor or binder maximum.
റീലുകളും കൈകാര്യം ചെയ്യലും
Input/output reel dimensions and weight, clamping, lifting and traverse.
The supplied reference uses 12 loose-tube pay-offs. Final tube range, lay, binding speed, line speed, output drum and installed power belong in the agreed technical schedule—not an assumption based on the model name.
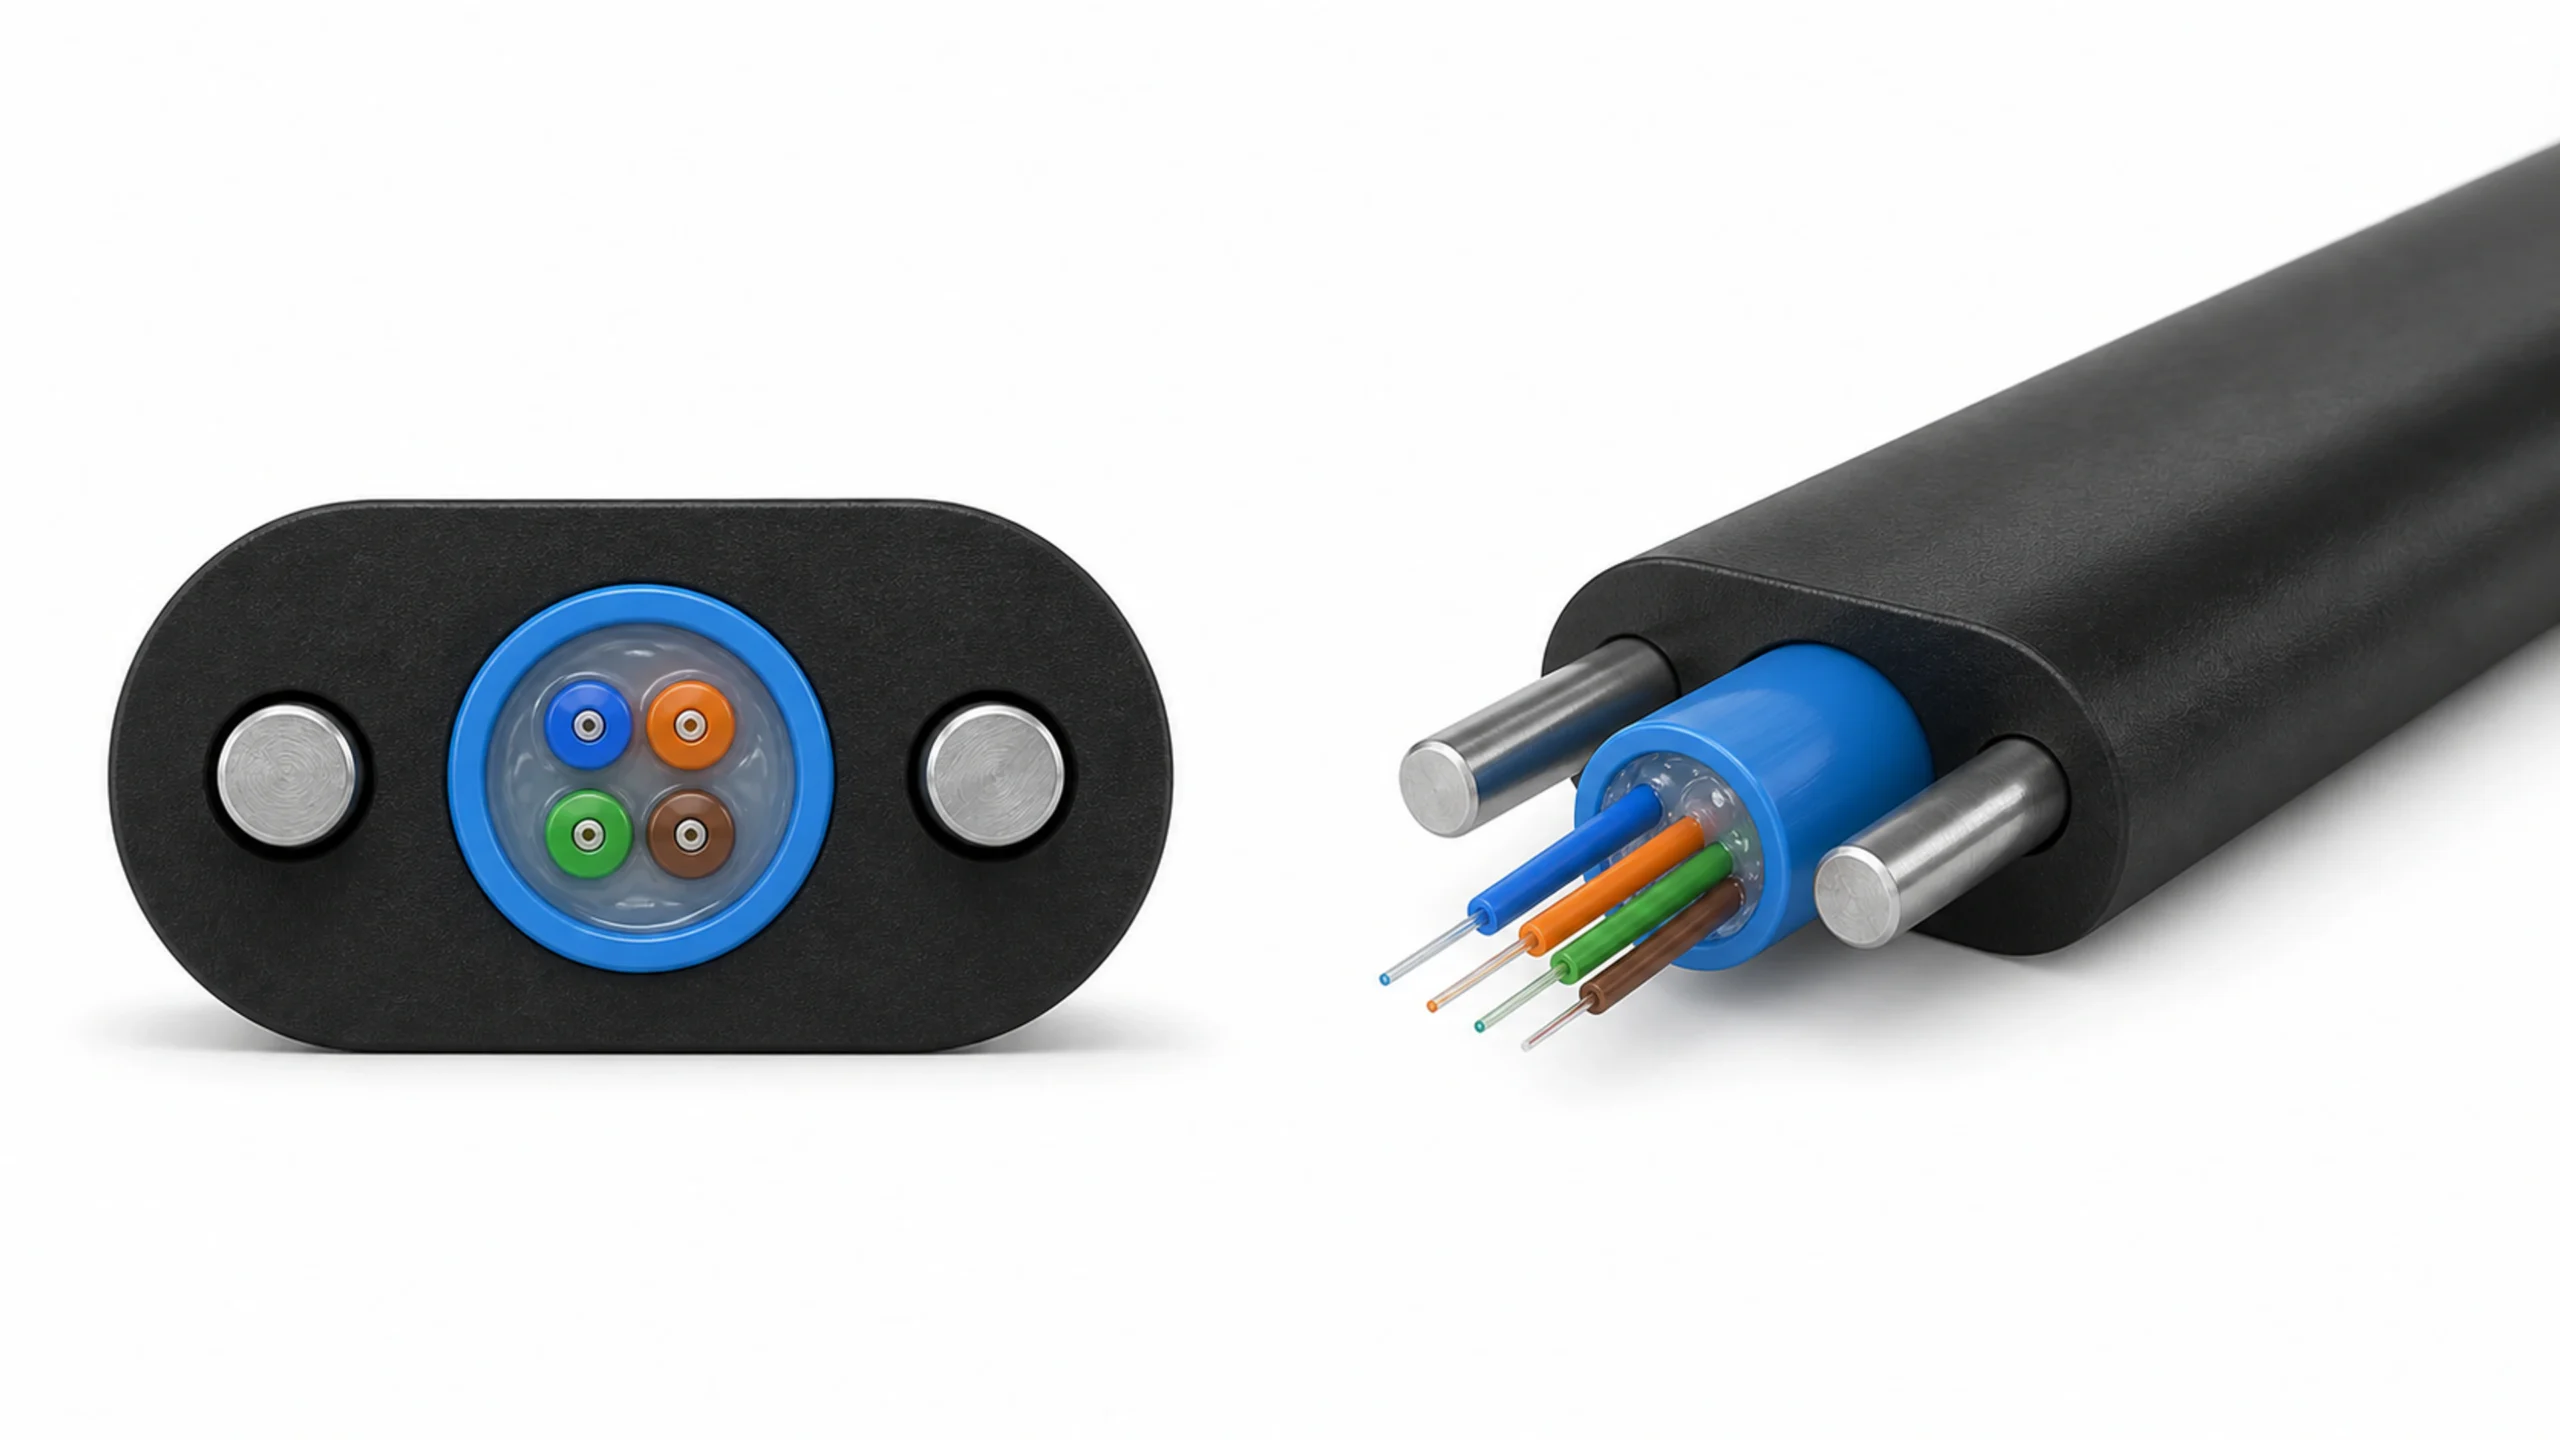
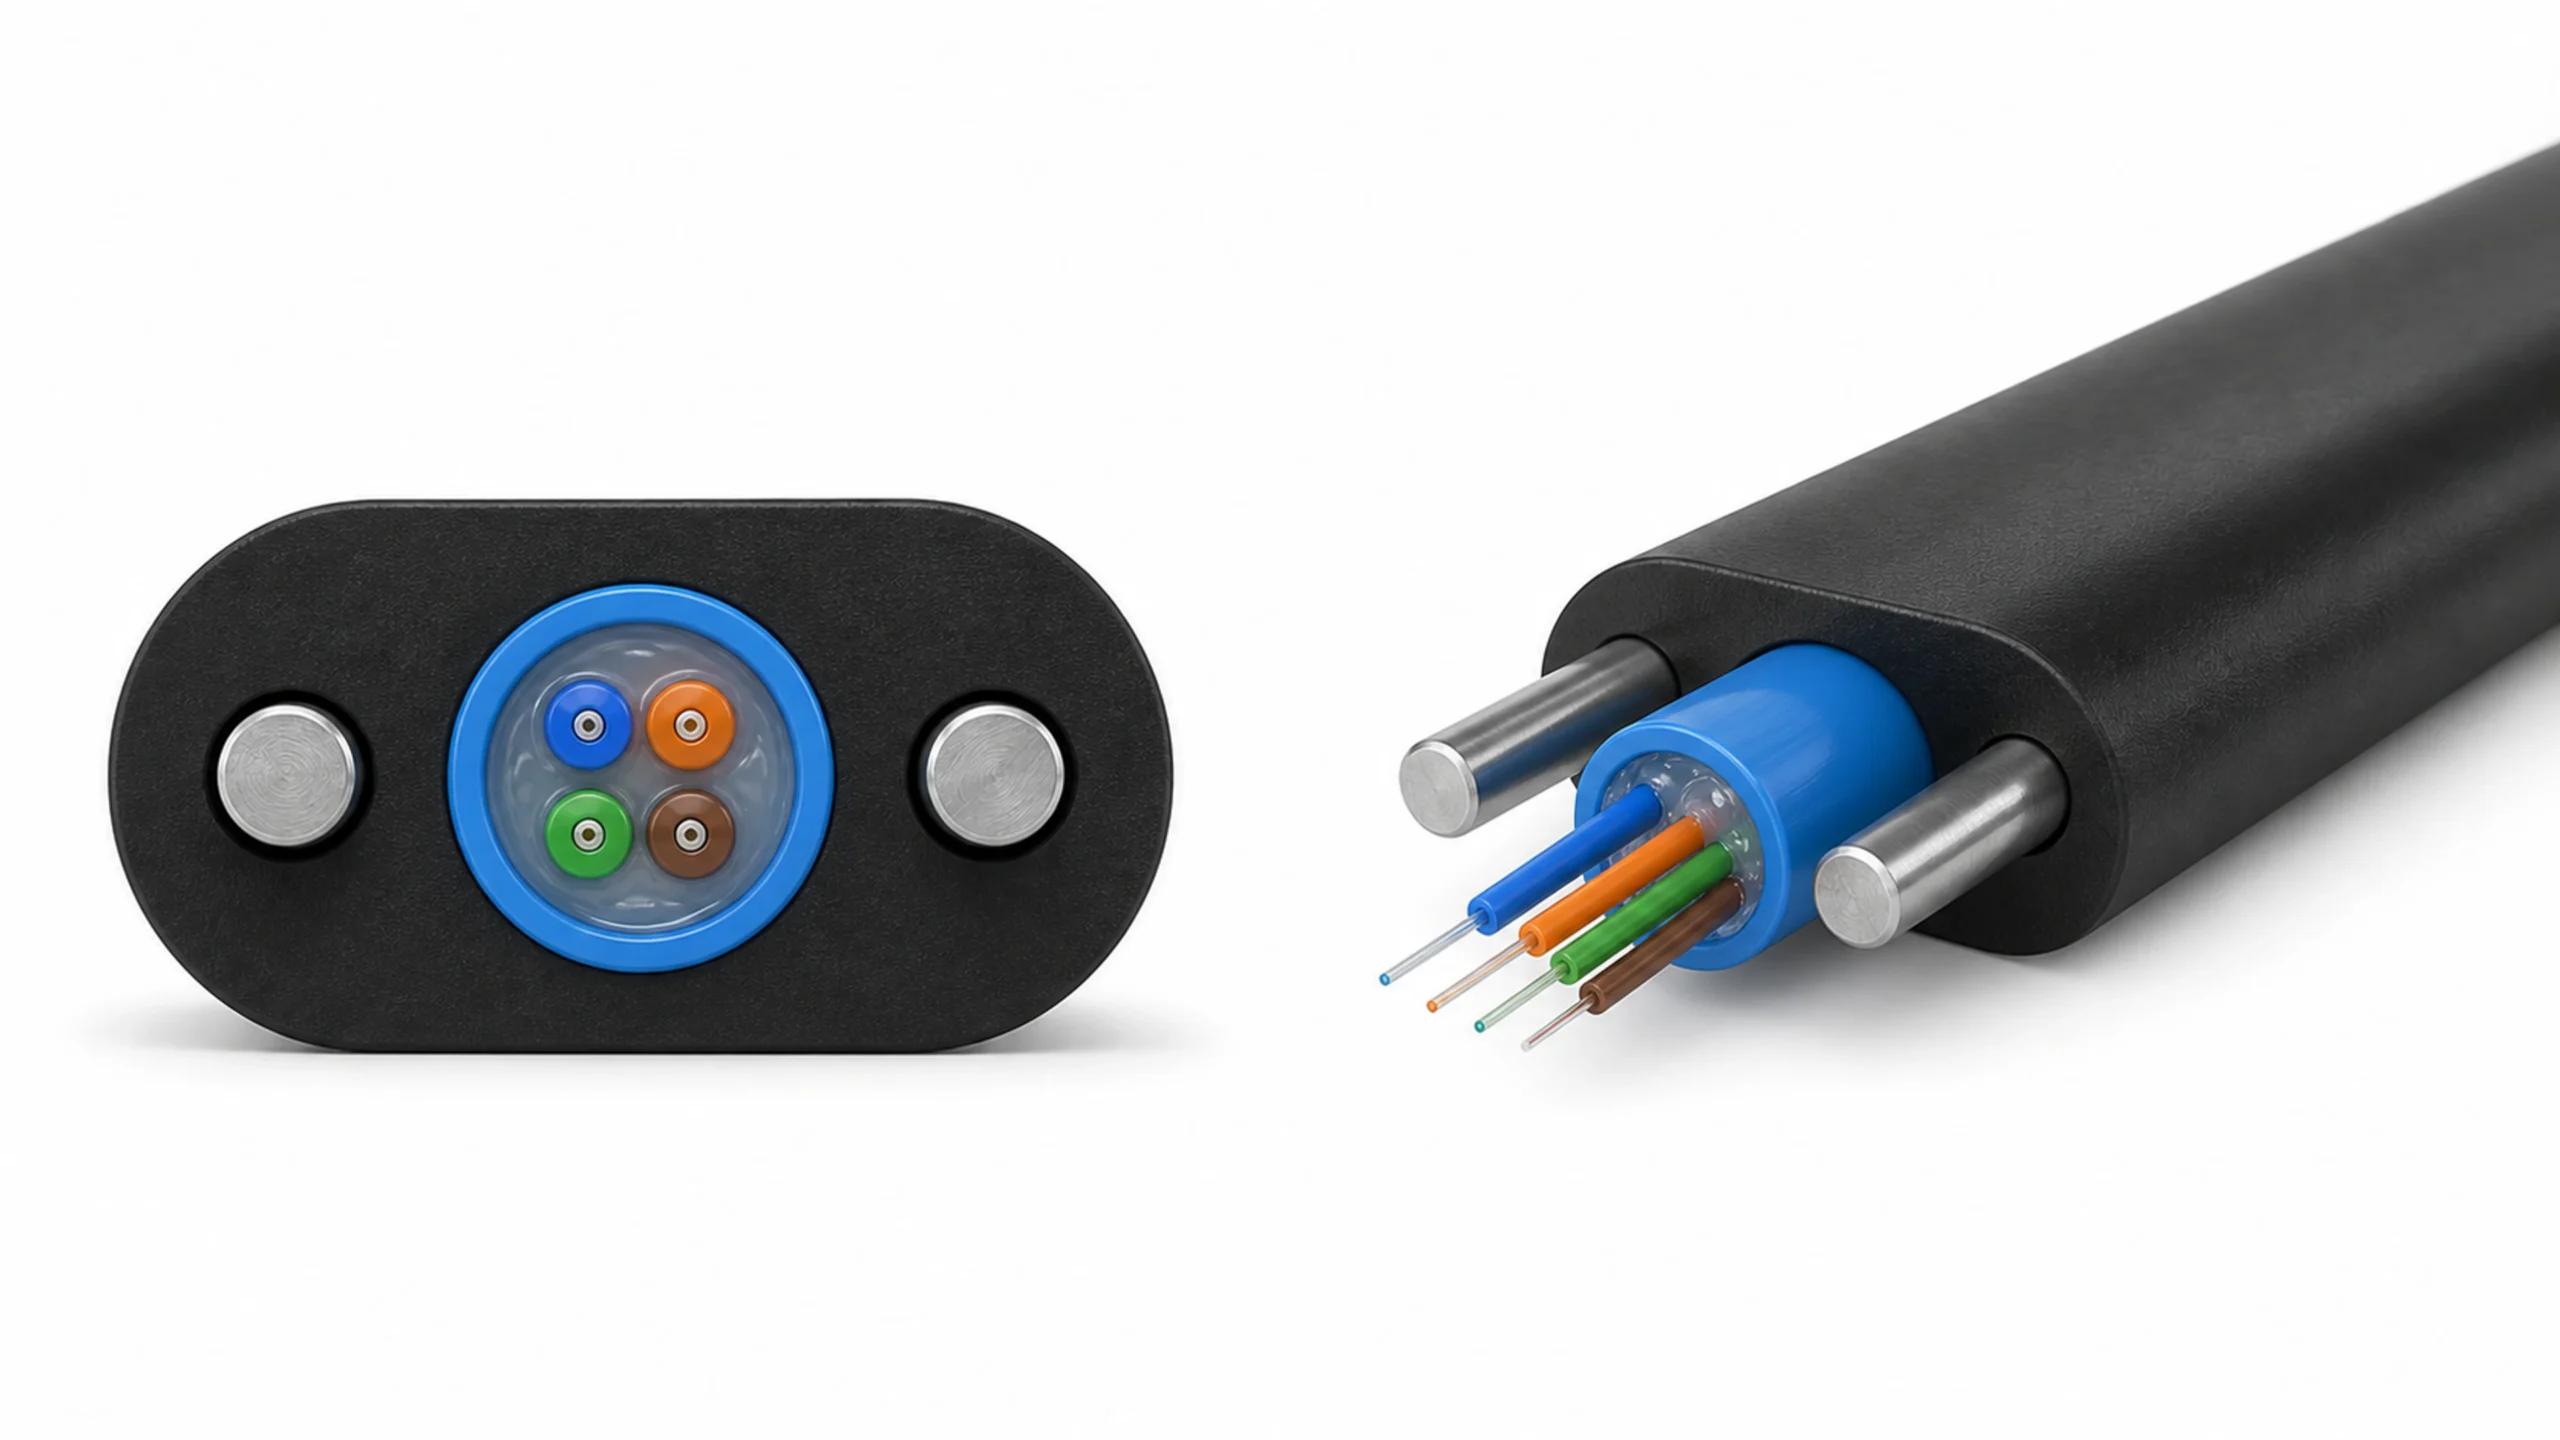
Construction matters: a central-tube cable does not automatically require this standalone SZ line. The linked Figure-8 page describes its particular stranded construction, not every cable sold under a similar name.
Watch the process. Define what the trial must demonstrate.
The HONGKAI HK-800/12 video supports a discussion of equipment and operating sequence. It is not a capacity guarantee or an acceptance record for a new project.
01PRODUCT
Trial the specified construction.
Use agreed tubes, central member, binding materials and reels.
02PROCESS
Check coordinated behavior.
Observe pay-off tension, SZ reversal, binding, traction and start/stop sequence.
03OUTPUT
Agree the inspection record.
Confirm core geometry, lay, winding and the required optical or other checks against the written test method.
ACCEPTANCE BASISഅംഗീകൃത ഡ്രോയിംഗ് + യോജിച്ച മെറ്റീരിയലുകൾ + പ്രവർത്തന സാഹചര്യങ്ങൾ + എഴുതിയ പരിശോധനാ രീതി
Define the support around the equipment—not only the machine list.
എഴുതിയ നിർദ്ദേശം ഉപകരണ തിരഞ്ഞെടുപ്പ്, ഏകീകരണം, സ്റ്റാർട്ട്-അപ്പ് ഉത്തരവാദിത്തങ്ങൾ എന്നിവ തമ്മിൽ ബന്ധിപ്പിക്കണം. HONGKAI ഉമായി നിങ്ങളുടെ പദ്ധതിയുടെ പരിധി സ്ഥിരീകരിക്കുക.
01
ഉപകരണ വ്യാപ്തി
നൽകിയിട്ടുള്ള മൊഡ്യൂളുകളും അളവുകളും സpecified ചെയ്യുക
Identify retained and buyer-supplied equipment
ഉപകരണ-സ്രോതസ്സ് ഉത്തരവാദിത്തങ്ങൾ രേഖപ്പെടുത്തുക
02
Line integration
ലേഔട്ടും മെറ്റീരിയൽ-ഫ്ലോ ഇന്റർഫേസുകളും അവലോകനം ചെയ്യുക
നിയന്ത്രണങ്ങൾ, സൗകര്യങ്ങൾ, സുരക്ഷാ അതിർത്തികൾ എന്നിവ നിർവചിക്കുക
Agree installation and commissioning scope
03
ആരംഭവും പിന്തുണയും
Define trial products and acceptance records
ഓപ്പറേറ്റർ പരിശീലനവും രേഖകളും സ്ഥിരീകരിക്കുക
Agree spare-parts and after-sales scope
09START THE ENGINEERING REVIEW
Tell us about the core you need to produce.
നിങ്ങളുടെ ഡ്രോയിംഗ്, ഉൽപ്പന്ന ആവശ്യകതകൾ അല്ലെങ്കിൽ നിലവിലുള്ള ഉപകരണങ്ങൾ ഉപയോഗിച്ച് ആരംഭിക്കുക. ആദ്യ റിവ്യൂ സമയത്ത് സാങ്കേതിക വിശദാംശങ്ങൾ സ്ഥിരീകരിക്കാം.
WHAT TO PREPARE
Nine inputs for an SZ line review.
01
Cable and cable-core drawings
02
Tube count, sizes and supply reels
03
Central member and filler details
04
Binding and water-blocking materials
05
Pitch and reversal requirements
06
Output reel and handling requirements
07
Target output and operating plan
08
Factory layout and retained equipment
09
Quality checks and acceptance conditions
10BUYER FAQ
Questions before specifying an SZ line.
Review the cable construction, equipment boundary and information needed for a proposal.
01ഒരു ഒപ്റ്റിക്കൽ കേബിൾ SZ സ്ട്രാൻഡിംഗ് ലൈൻ എന്താണ് ഉത്പാദിപ്പിക്കുന്നത്?
ഇത് യോഗ്യതയുള്ള ലൂസ് ട്യൂബുകളിൽ നിന്നും നിർദ്ദിഷ്ട സെൻട്രൽ മെമ്പറിൽ നിന്നും ഒരു സ്ട്രാൻഡഡ് കേബിൾ കോർ രൂപീകരിക്കുന്നു, നിർമ്മാണത്തിന് ആവശ്യമായ ബൈൻഡിംഗും വാട്ടർ-ബ്ലോക്കിംഗ് പാക്കേജും ഉൾപ്പെടുത്തി. ഫൈനൽ റീയിൻഫോഴ്സ്മെന്റ്, ആർമറിംഗ്, ഷീത്തിംഗ് എന്നിവ പ്രത്യേക ഘട്ടങ്ങളാണ്, എഴുതിയ സ്കോപ്പ് അവ സംയോജിപ്പിക്കുന്നില്ലെങ്കിൽ.
02ഏതൊക്കെ കേബിൾ പരിഹാരങ്ങൾക്ക് ഈ ഘട്ടം ഉൾപ്പെടുത്താൻ കഴിയും?
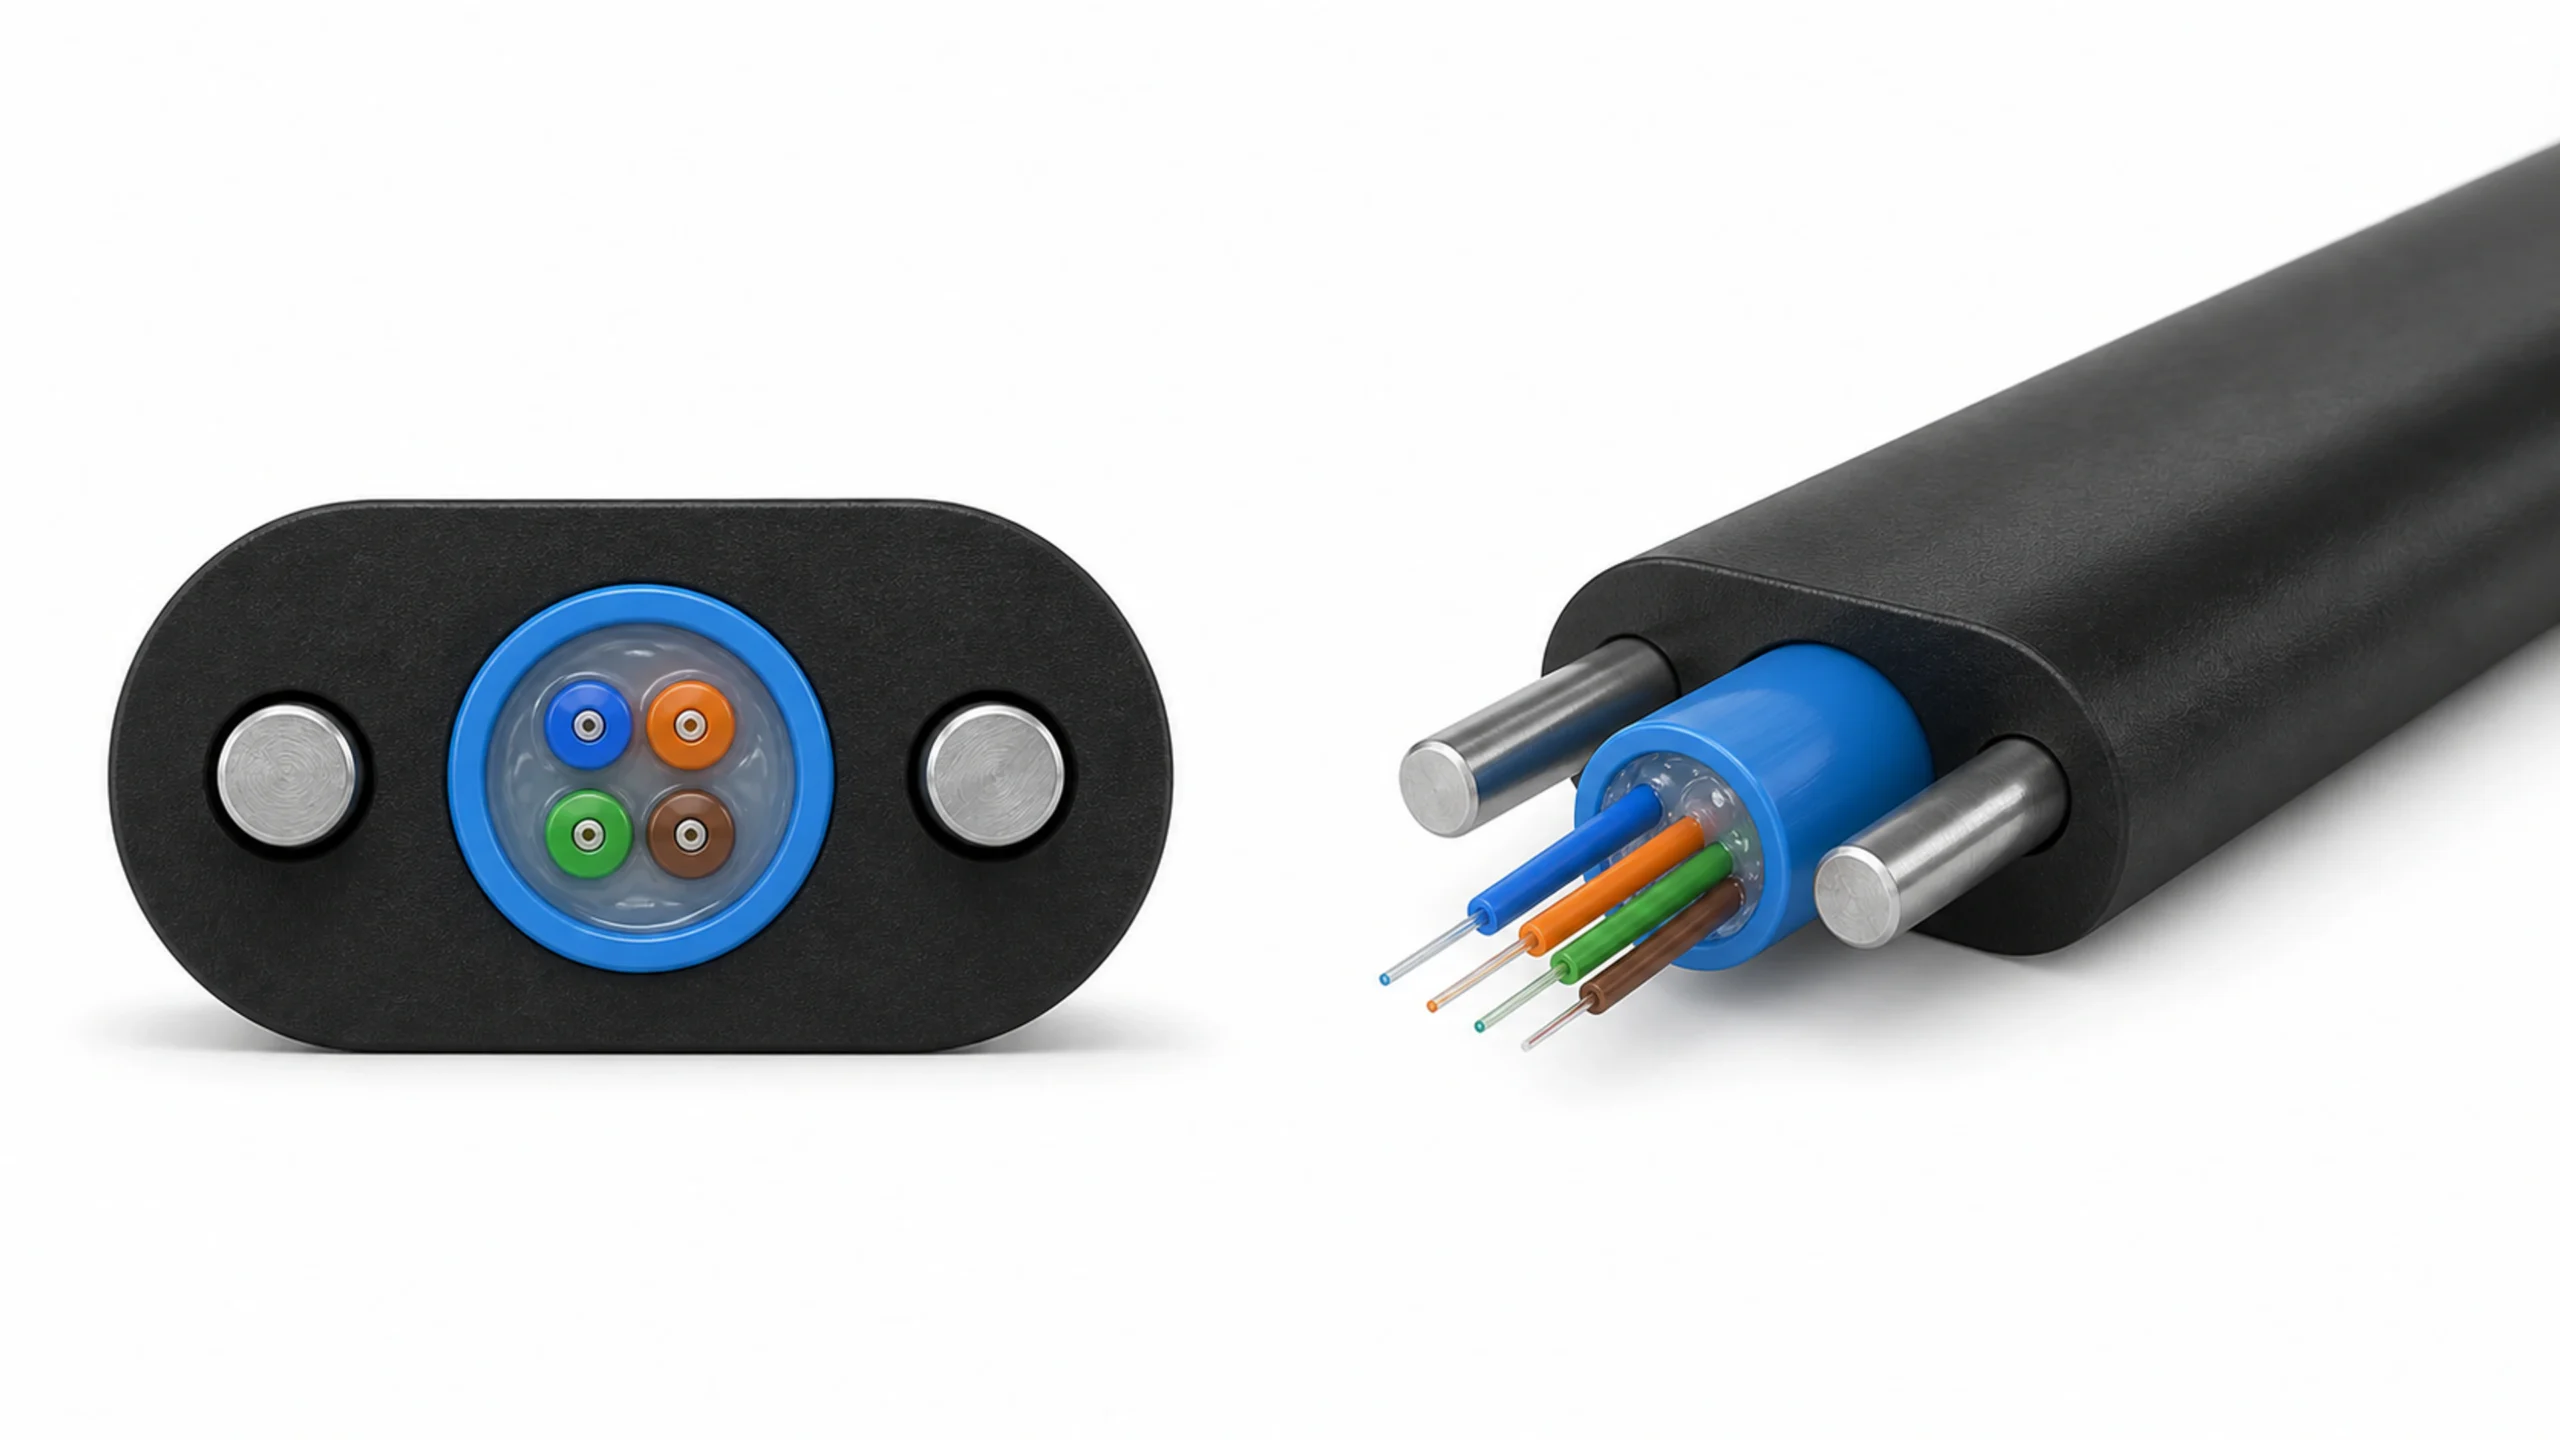
ബന്ധിപ്പിച്ച ADSS, മൈക്രോ കേബിൾ, GYXTC8S റഫറൻസ് നിർമ്മാണങ്ങൾ SZ കോർ സ്ട്രാൻഡിംഗ് ഉൾപ്പെടുത്തുന്നു. യോജിപ്പ് അവയുടെ യഥാർത്ഥ ട്യൂബ് എണ്ണം, കോർ ജ്യാമിതി, മെറ്റീരിയലുകൾ, പ്രക്രിയാ ആവശ്യങ്ങൾ എന്നിവയെ ആശ്രയിച്ചിരിക്കുന്നു. ഒരു പൊരുത്തപ്പെടുന്ന കേബിൾ പേര് മാത്രം അനുയോജ്യതയുടെ സ്ഥിരീകരണമല്ല.
03HK-800/12 എന്നത് ഏക സാധ്യമായ കോൺഫിഗറേഷനാണോ?
HK-800/12 ഉപകരണം വിശദീകരിക്കാൻ ഉപയോഗിക്കുന്ന നൽകിയിട്ടുള്ള പ്രൊജക്റ്റ് റഫറൻസാണ്. ഒരു പ്രസ്താവനയിൽ സജീവ ട്യൂബ് എണ്ണം, ഇൻപുട്ട്, ഔട്ട്പുട്ട് പാക്കേജുകൾ, ഓസിലേറ്റർ, ബൈൻഡിംഗ് സിസ്റ്റം, നിയന്ത്രണങ്ങൾ, ആവശ്യമായ ഓപ്പറേറ്റിംഗ് എൻവലപ്പ് എന്നിവ നിർവചിക്കണം. മറ്റ് കോൺഫിഗറേഷനുകൾക്ക് എഞ്ചിനീയറിംഗ് സ്ഥിരീകരണം ആവശ്യമാണ്.
04പ്രദർശിപ്പിച്ചിരിക്കുന്ന ഉപകരണങ്ങളുടെ അളവുകൾ നിശ്ചിതമാണോ?
ഇല്ല. പാനോരമ ഉപകരണങ്ങളുടെ ക്രമീകരണവും മൊഡ്യൂൾ ലിസ്റ്റ് അതിന്റെ പ്രവർത്തനങ്ങളും വിശദീകരിക്കുന്നു. നൽകിയിട്ടുള്ള റഫറൻസ് പ്രൊപ്പോസലിൽ 12 ട്യൂബ് പേ-ഓഫുകൾ ലിസ്റ്റുചെയ്തിരിക്കുന്നു, എന്നാൽ പാനോരമ ലളിതമാക്കിയിരിക്കുന്നു. അളവുകൾ നിർണ്ണയിക്കുന്നതിന് അംഗീകൃത ഉപകരണ ലിസ്റ്റും ലേഔട്ടും ഉപയോഗിക്കുക.
05എല്ലാ നിർമ്മാണത്തിനും സംയുക്ത ഫില്ലിംഗും വാട്ടർ-ബ്ലോക്കിംഗ് ടേപ്പും ആവശ്യമാണോ?
നമ്പർ. കേബിൾ നിർമ്മാണത്തിൽ നിന്നും ബാധകമായ പ്രൊജക്റ്റ് ആവശ്യങ്ങൾക്കനുസരിച്ചും ഫില്ലിംഗ് കോമ്പൗണ്ട്, ബൈൻഡിംഗ് യാൺ, ടേപ്പ്, മറ്റ് സംരക്ഷണ മെറ്റീരിയലുകൾ തിരഞ്ഞെടുക്കുന്നു. അവയുടെ ഉപയോഗ സ്ഥാനങ്ങളും ഉപകരണങ്ങളും ഒരുമിച്ച് സ്ഥിരീകരിക്കണം.
06ഉത്പാദന വേഗത എങ്ങനെ താരതമ്യം ചെയ്യണം?
ഒരേ കേബിൾ ഡ്രോയിംഗ്, മെറ്റീരിയലുകൾ, പിച്ച്, റീൽ പാക്കേജ്, ട്രയൽ ദൈർഘ്യം, പരിശോധന രീതി എന്നിവ ഉപയോഗിക്കുക. പരമാവധി ഘടക വേഗതകൾ, സ്ഥിരമായ പൂർണ്ണ-ലൈൻ വേഗത, മാറ്റങ്ങൾക്ക് ശേഷമുള്ള നെറ്റ് ഔട്ട്പുട്ട് എന്നിവ വ്യത്യസ്ത അളവുകളാണ്.
07തിരഞ്ഞെടുത്ത മെഷീനുകൾ നിലവിലുള്ള ലൈനിൽ ഏകോപിപ്പിക്കാൻ കഴിയുമോ?
നിലനിർത്തിയ ഉപകരണങ്ങൾ ആദ്യം അവലോകനം ചെയ്യണം, അതിൽ അതിന്റെ മെക്കാനിക്കൽ അവസ്ഥ, നിയന്ത്രണ സിഗ്നലുകൾ, ലൈൻ ദിശ, സുരക്ഷാ ഇന്റർഫേസുകൾ, ലഭ്യമായ കപ്പാസിറ്റി എന്നിവ ഉൾപ്പെടുന്നു. തുടർന്ന് ഈ പ്രസ്താവന പകരം വയ്ക്കൽ പരിധിയും സ്വീകാര്യതാ അതിർത്തിയും നിർവചിക്കുന്നു.
08ആദ്യ പ്രൊപ്പോസലിനായി ഞാൻ എന്താണ് അയയ്ക്കേണ്ടത്?
ലഭ്യമായ കേബിൾ ഡ്രോയിംഗ്, ട്യൂബ്, റീൽ വിവരങ്ങൾ, കോർ നിർമ്മാണം, ഉത്പാദന ലക്ഷ്യം, ഫാക്ടറി സന്ദർഭം എന്നിവ അയയ്ക്കുക. അറിയാവുന്നെങ്കിൽ ബൈൻഡിംഗ്, വാട്ടർ-ബ്ലോക്കിംഗ് ആവശ്യകതകളും ചേർക്കുക. കാണാതായ വിവരങ്ങൾ എഞ്ചിനീയറിംഗ് റിവ്യൂവിനായി തുറന്നു വയ്ക്കാം.
We've detected you might be speaking a different language. Do you want to change to:





 English
 हिन्दी
 فارسی