


A cable factory owner may be offered a single-screw extruder, a twin-screw extruder, or a proposal that uses both terms without defining the process boundary. The important decision is not whether two screws sound more advanced. It is whether the factory needs to apply an approved compound to a conductor or cable, manufacture the compound itself, or do both as separate production stages.
For most insulation and sheathing projects that begin with qualified cable compound, the main production duty is stable cable coating through a crosshead, supported by pay-off, preheating where required, cooling, measurement, testing, traction and take-up. Twin-screw equipment belongs primarily to a compounding process when the factory must feed, disperse, homogenize, vent and pelletize a formulation. A compounding line does not remove the need for a correctly specified cable-coating line.

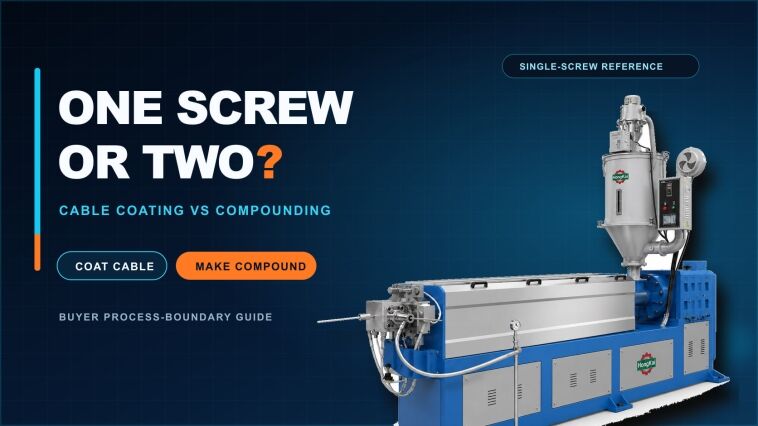
케이블 코팅 압출기의 HONGKAI 레퍼런스 렌더링입니다. 이 이미지는 투스크류 컴파운딩 플랜트를 나타내지 않으며, 두 공정 경로가 상호 교환 가능하다는 것을 의미하지 않습니다.
This guide is for factory owners, production managers and technical procurement teams deciding what belongs in an extrusion quotation. It compares process duty, incoming material, finished output, auxiliary equipment and acceptance evidence so that screw count does not replace a complete production specification.
컴파운드 제조에서 케이블 코팅 분리
A single-screw-versus-twin-screw comparison is meaningful only after the buyer states what enters the process and what must leave it. Applying insulation or sheath around a moving conductor is a different production boundary from turning polymers, fillers and additives into a controlled cable compound.
The cable-coating boundary starts with an approved material in a defined supply form. The material is prepared as required, melted and delivered through a crosshead around a conductor, insulated core or cable core. The output is a continuously coated wire or cable that must meet dimensional, surface, electrical and handling requirements.
The compounding boundary starts with a formulation and controlled ingredient streams. The process may include feeding, premixing, plasticizing, dispersive and distributive mixing, venting, filtration, pressure building, pelletizing, cooling and packaging. The output is normally an identified compound lot that still needs qualification and must later be processed on the cable extrusion line.
| 공정 경계 | 일반적인 입력 상태 | Required output | 장비가 입증해야 하는 사항 |
|---|---|---|---|
| 케이블 절연 또는 외피 | 승인된 펠릿, 과립 또는 기타 공급업체 자격을 갖춘 원료 | 지정된 패키지의 피복 도체 또는 케이블 | 안정적인 치수, 표면, 층의 무결성, 필요한 온라인 검사 및 제어된 권취 |
| 색상 스트라이프 또는 추가 케이블 레이어 | 별도의 층을 위한 승인된 재료 | 케이블의 정의된 스트라이프 또는 공압출층 | 층 위치, 연속성, 치수, 해당 시 접착력 및 반복 가능한 제어 |
| 케이블 혼합물 생산 | 처방에 의해 정의된 제어된 수지, 충전제, 첨가제, 액체 또는 프리믹스 | 적격한 펠릿 또는 기타 승인된 혼합 형태 | 성분 제어, 혼합, 배기, 열 이력, 로트 균일성 및 후속 공정성 |
| 통합 소재 및 케이블 프로젝트 | 원료 및 도체 또는 케이블 입력 | 자격을 갖춘 컴파운드 및 별도로 승인된 완제 케이블 | 연결되어 있지만 구분되는 두 개의 릴리스 패키지: 재료 증거 및 케이블 증거 |
The official Coperion cable-compound process illustrates the distinction clearly. Its two-stage system uses a twin-screw section for plasticizing, mixing and homogenizing, then a single discharge screw and pelletizing system for the compound-production duty.1 해당 탠덤 시스템의 단일 스크류는 케이블 크로스헤드 라인과 동일한 생산 경계가 아니며, 컴파운드 공장을 떠나는 펠릿은 완제 케이블이 아니다.
Decision criterion: Write one sentence for each proposed extruder: “This machine receives [named input] and produces [named output].” If the supplier cannot complete that sentence with a physical input, a controlled output and named acceptance evidence, the screw-count comparison is premature.
For HONGKAI cable-line scoping, the first practical input is the material the buyer intends to run. The material identity alone is still incomplete: the buyer must also state the cable construction and required output so that machine size and screw design can be reviewed together. A separate compounding review begins only when the project input is a formulation or multiple controlled ingredients rather than a ready-to-process cable compound.
동일한 차원에서 두 경로를 비교하세요
Single-screw cable coating and twin-screw compounding should be compared by process responsibility, not by a generic claim that one mixes better or runs faster. Each route is optimized around a different transformation and requires different upstream, downstream and quality systems.
| 비교 기준 | 단일 스크류 케이블 코팅 라인 | 쌍축 압출 혼합 공정 |
|---|---|---|
| Primary duty | 승인된 컴파운드를 용융하여 케이블 크로스헤드에 안정적으로 공급합니다. | 정의된 혼합 공정을 통해 여러 배합 성분을 결합하고 제어합니다. |
| 주요 생산 투입물 | 적격한 케이블 컴파운드 및 도체, 절연된 코어 또는 케이블 코어 | 수지, 충전제, 첨가제, 액체, 프리믹스 또는 기타 배합 원료 |
| 주요 생산 산출물 | 절연 전선, 코팅된 도체 또는 피복 케이블 | 후속 케이블 가공을 위한 컴파운드 로트(일반적으로 펠릿 형태) |
| Mixing requirement | 안정적인 용융 상태를 유지하고 승인된 컴파운드를 가공 윈도우 내에서 보존하십시오. | 통제된 성분으로부터 지정된 분산성, 분포 및 균일성을 생성합니다. |
| 압력 및 성형 작업 | 연속적으로 이동하는 케이블 제품 주위에 층을 형성하는 크로스헤드에 재료를 공급합니다 | 다이와 하류의 컴파운드 처리 또는 펠릿화 시스템에 원료를 공급합니다. 일부 시스템은 혼합과 압력 상승 과정을 분리합니다. |
| 필수 주변 장비 | 페이오프, 필요 시 정렬 또는 예열, 크로스헤드 및 공구, 냉각, 게이지, 테스터, 캡스턴, 애큐뮬레이터 및 테이크업 | 원료 저장, 정밀 투입기, 필요 시 혼합기, 사이드 피딩, 액체 정량 주입, 배기, 여과, 펠릿화, 냉각 및 로트 취급 |
| 코어 수용 물체 | 기록된 안정 상태에서 제작된 식별된 케이블 샘플 | 추적 가능한 원료와 통제된 처방으로 만든 식별된 복합 로트 |
| 일반적인 확장 질문 | 동일한 라인이 다른 승인된 케이블 구조, 재질 등급, 레이어 또는 패키지를 가공할 수 있습니까? | Can the plant produce another qualified formulation without compromising feeding, mixing, venting, cleaning or lot control? |
이 구분은 또한 세 가지 일반적인 명명 오류를 방지한다.
A current Maillefer component index maps screw-diameter extruders to insulation and sheathing duties across building wire, low-voltage, telecom, fiber-optic and other cable applications.2 해당 참조 자료는 케이블 코팅 경계를 지원하지만, 나사 직경만으로 선택 방법이 되지는 않는다.
First, a main extruder plus a small color-stripe extruder is not a twin-screw extruder. It is a multi-extruder cable line in which separate single-screw units feed different material streams or layers into compatible tooling.
In that arrangement, the main extruder and color-stripe extruder meet at the crosshead. The required stripe proportion is one of the inputs used to size the auxiliary extruder; the presence of two extruder bodies does not establish a twin-screw process.
Second, a multilayer crosshead supplied by two or three extruders does not make those extruders a twin-screw machine. The buyer must specify each layer, material, flow path, interface and control duty independently.
Third, a twin-screw feeder is not automatically a twin-screw process extruder. Ingredient feeding and polymer compounding are separate equipment functions, even when both use rotating screws.
Common mistakes: A quotation uses “double extruder,” “co-extrusion,” “twin screw” and “two-color line” as interchangeable terms. The buyer should require a process diagram that shows the number of extruder barrels, the screw arrangement inside each barrel, the material entering each unit and the die or crosshead receiving each melt stream.
자재 상태 및 판매 가능 제품에서 경로를 선택하세요
The most reliable selection starts with the approved material supply strategy and the first saleable cable. A factory buying qualified compound needs a different project from a factory developing and manufacturing its own cable formulations.
기계 모델을 요청하기 전에 이 순서를 사용하세요:
- 첫 번째 케이블 구조, 레이어 순서, 도체 또는 코어 입력, 완성 패키지 및 승인 기준을 확정합니다.
- 승인된 등급과 공급 형태별로 각 절연체, 시스(피복), 스트라이프 또는 기타 적용 재료에 이름을 표시하십시오.
- 공장이 적격 컴파운드를 구매할지, 자체적으로 관리된 컴파운드를 생산할지, 또는 두 가지 방식을 별도로 평가할지를 결정한다.
- Map every physical transformation from incoming material to compound lot and from compound lot to finished cable.
- Build separate factory acceptance test plans for any process boundary that creates a separately controlled output.
| Buyer situation | 예비 경로 | 아직 확인이 필요한 경계 |
|---|---|---|
| 공장은 승인된 펠릿을 구매하여 절연층 또는 시스층을 하나 적용합니다. | 승인된 제품 및 재료 주위에 케이블 코팅 라인을 지정하십시오. | 스크류 설계, 배럴, 크로스헤드, 공구, 냉각 장치 및 보조 장비는 정확한 재료와 케이블에 맞아야 한다. |
| 케이블에는 컬러 스트라이프 또는 두 번째 재료 스트림이 필요합니다. | Review a separate auxiliary extruder and compatible crosshead or die arrangement | 이것은 다중 압출 작업이지, 이중나사 압출 공정이 필요하다는 증거가 아닙니다. |
| The factory wants to blend resin, fillers and additives into its own commercial compound | 케이블 라인 전에 전용 혼합 프로젝트를 범위 설정하세요. | Formulation ownership, feeding, mixing, venting, pelletizing, laboratory release and liability must be written |
| 공장은 재생 또는 가변 재료를 사용하고자 합니다. | Do not select by screw count alone | Input variability, contamination, filtration, degradation, qualification and finished-cable limits require a controlled development plan |
| 이 프로젝트는 열감응성이며 고충전된 반응성 발포 고무 또는 가교결합 가능한 시스템을 사용한다. | Treat the process as material- and product-specific | Obtain material-supplier processing requirements and define residence time, shear, temperature, venting, curing or foaming controls as applicable |
| 공급업체는 다양한 PVC, PE, XLPE 또는 저연기 배출 조성물에 대해 하나의 라인을 제안합니다. | Keep compatibility provisional | 각 정확한 컴파운드 등급, 스크류, 툴링, 드라이어 또는 로더 요구사항, 클리닝 경로 및 승인 샘플을 검토해야 한다. |
“PVC,” “PE,” “XLPE” or “LSZH” is not a complete machine input. Commercial grades can differ in additives, fillers, moisture sensitivity, thermal limits, rheology, crosslinking route and required processing controls. A supplier should not convert a material family name into a universal screw geometry or output promise.
The HONGKAI project sequence is to match the required production output to a practical extruder size, then review the intended material against the screw design and the rest of the line. A dryer or additional feeding system is not added merely because the material name changes; those modules remain conditional on the exact grade, supply form and material-supplier processing guidance. The current Φ70 and Φ90 references therefore do not prove universal grade or brand compatibility.
The same caution applies to in-house formulation. Owning a twin-screw compounder creates responsibilities for recipes, ingredient verification, dosing accuracy, lot traceability, laboratory testing, change control, cleaning, nonconforming material and the interaction between compound quality and cable quality. It is a material-manufacturing decision, not merely an extra machine added to the extrusion hall.
Foaming and crosslinkable compounds require their own material-and-screw review because their raw-material behavior and test route differ from ordinary cable compounds. HONGKAI does not extend that confirmed boundary to recycled material or every high-fill low-smoke grade without the exact material data and a representative trial plan.
Red flags: A supplier recommends twin-screw equipment only because the buyer mentions additives; promises that “more mixing” will solve an undefined surface or electrical defect; or quotes a cable line before the compound grade, conductor, layer thickness, package and test basis are available.
스크류 수뿐만 아니라 전체 라인을 명시하십시오
A useful cable-extrusion quotation must connect the extruder to the conductor path, crosshead, cooling, measurement, traction, testing and take-up. A useful compounding quotation must connect raw-material control to feeding, mixing, venting, discharge, pelletizing, laboratory release and lot handling.
케이블 코팅 프로젝트의 경우, 구매자는 다음 입력사항을 포함한 제품 및 공정 문서를 제공해야 합니다:
| Input group | 기술 검토를 위한 최소 정보 |
|---|---|
| Finished cable | 도면, 레이어 순서, 공칭 및 관리 치수, 표면 요구사항, 마킹 및 포장 |
| 도체 또는 케이블 코어 | 재질, 구조, 입구 직경 또는 범위, 릴 치수, 허용 장력 및 표면 상태 |
| Applied compound | 공급업체 및 등급(가능한 경우), 공급 형태, 색상, 가공 지침, 건조 또는 전처리 요구사항, 로트 관리 |
| Extrusion duty | 절연체, 시스, 베딩, 스트라이프 또는 기타 명명된 층; 재료 공급 라인 수; 툴링 개념; 요구되는 라인 방향 |
| Online control | 직경 또는 벽두께 제어 방법, 해당 시 스파크 테스트, 인쇄 또는 마킹 검증, 길이 측정 및 추적성 |
| Factory interface | 전원, 냉각수, 필요 시 압축 공기, 배수, 평면도, 리프팅 및 릴 이동, 환경 제어 장치 및 기존 장비 |
| 수락 | 제품 출시, 재료 로트, 목표 운전 조건, 측정, 시험 방법, 보관 기록 및 미해결 사항 처리 절차 |
HONGKAI’s verified Φ70 insulation-line and Φ90+50 sheathing-line configuration documents show single-screw cable-coating references with separate material handling, crosshead, cooling, measurement, traction and take-up functions. The “+35” or “+50” designation in these references identifies an additional color-stripe extruder; it does not describe an intermeshing twin-screw barrel. Final screw, barrel, tooling, material and line scope remain project-specific.
For a color-stripe request, the buyer should also define the stripe proportion and visible result. That input affects the auxiliary-extruder size and crosshead arrangement; it should not be translated into a generic request for a “twin-screw cable extruder.”
공개된 HONGKAI 케이블 피복 라인 마찬가지로 페이오프, 크로스헤드, 냉각, 직경 측정, 트랙션 및 테이크업을 포함하는 보다 긴 라인 내의 하나의 스테이션으로 압출기를 제시한다. HONGKAI 저압 생산 가이드 승인된 케이블 레이어와 필요한 경로에서 시작되며, 압출기 모델을 완전한 공장으로 간주하지 않는다.
유지보수 또는 교체 작업을 위해 HONGKAI 케이블 압출 부품 페이지 lists the measurements needed to confirm a screw and barrel, including diameter, length or L/D information, thread form and material requirement. Those replacement inputs are also useful during a new-line review, but dimensional compatibility alone still does not prove process suitability.
Note: Current HONGKAI evidence supports the cited single-screw cable-coating configurations. It does not by itself establish a HONGKAI twin-screw compounding model, formulation package or compound-performance guarantee. Any in-house compounding scope must identify the responsible specialist, formulation owner, supplied modules and acceptance boundary in writing.
컴파운드 및 케이블에 대해 별도의 FAT 증거 자료를 작성하세요.
Factory acceptance should prove the output of each production boundary. A compounder must release an identified material lot against the agreed formulation and test plan; a cable line must run an identified product at a stable recorded condition and release the cable against the agreed dimensional, electrical, mechanical and handling checks.
| Evidence layer | 케이블 코팅 라인 FAT | 컴파운딩 라인 FAT |
|---|---|---|
| Controlled inputs | 승인된 도체 또는 케이블 코어, 컴파운드 로트, 공구 및 포장 | 승인된 제조처방 개정본, 원료 로트, 투입기 및 계량 기록 |
| Process record | 온도 구역, 스크류 및 라인 상태, 용융 또는 공정 관찰, 트랙션, 냉각 및 관련 경보 | 적용 가능한 경우 공급 속도, 스크류 구성 및 상태, 온도, 토크 또는 부하, 배기, 압력, 여과 및 펠릿화 조건 |
| Physical output | 합의된 릴 또는 포장에 식별된 절연 또는 시스 케이블 | 합의된 펠릿 또는 재료 형태로 식별된 혼합 로트 |
| Immediate checks | 치수, 동심도 또는 필요 시 벽 두께 확인, 표면, 마킹, 온라인 테스트 및 권선 품질 | 외관, 펠릿 또는 출력 일관성, 오염 제어 및 합의된 실험실 시료 식별 |
| Release evidence | 케이블 드로잉, 표준 또는 관리 계획과 연계된 제품별 시험 | 성분 사양 및 후속 가공 요구사항과 연계된 재료 시험 |
| Traceability | 케이블 드럼에서 도체/코어, 복합 로트, 설정, 시험 및 작업자 기록에 이르기까지 | 복합 로트를 원료, 처방 변경, 설정, 샘플, 시험 및 처분과 연결 |
| Handover | 합의된 레시피 또는 설정, 공구 목록, 도면, 매뉴얼, 경보 설정, 교육 및 미해결 사항 | Formulation responsibility, screw configuration record, feeder calibration, cleaning/changeover method, lab methods, traceability and open items |
Open-head output is not enough to accept a cable line. It does not prove that the selected conductor, crosshead, tooling, cooling path, measurement system, traction and take-up can produce the agreed cable continuously. Likewise, a short cable sample cannot prove a compound plant if ingredient control, lot uniformity, venting, filtration, pellet condition and laboratory release remain undefined.
HONGKAI uses two different checks for the cable-extrusion duty. First, the head is opened and the extruder output is weighed under the agreed full-speed test condition to record kilograms per hour. Second, the complete line runs the customer’s specified cable under the agreed full-speed condition to record metres per minute while the finished dimensions and other signed accuracy requirements remain within tolerance. The first check verifies extrusion output; the second verifies that the complete line can make the agreed product. Neither result should substitute for the other.
구매자는 다음 최종 검토 체크리스트를 사용하여 두 경로 중 어느 쪽이든 승인하기 전에 확인할 수 있습니다.
- ☐ 모든 압출기의 공정 입력 및 출력에 이름이 지정되어 있다.
- ☐ “싱글”, “트윈”, “코엑스트루전” 및 “컬러 스트라이프”가 공정 다이어그램과 장비 목록에서 일관되게 사용됩니다.
- ☐ 정확한 재료 등급 또는 통제된 조성식이 일반적인 중합체 계열 표현을 대체한다.
- ☐ Upstream and downstream modules are included with their interfaces and responsible supplier.
- ☐ Cable-coating FAT and compound-production FAT have separate samples, records and release criteria.
- ☐ Future materials or cable families are listed as optional scope until representative trials and evidence are agreed.
- ☐ HONGKAI-manufactured equipment, integrated specialist equipment and buyer-supplied systems are separated in the responsibility matrix.
The correct choice is therefore not “single screw or twin screw” in isolation. It is a verified route from the buyer’s material state to the first saleable cable, with every transformation, interface and acceptance record assigned to the correct production boundary. Twin-screw compounding is included here as buyer education, not as evidence of a current HONGKAI compounding-machine offer. If a project includes pellet production, the specialist compound-equipment and formulation scope must be defined separately from the HONGKAI cable-coating line. The same input dossier can be submitted through the clean HONGKAI project intake page 케이블 코팅, 재료 준비 및 특수 혼합 작업 범위가 별도로 검토되도록 하기 위해.
-
Coperion, STS Mc11 two-stage compounder for cable compounds, 케이블 복합재 생산 시스템 하나로 공급, 이중 나사 혼합 및 균질화, 단일 배출 나사로의 이송, 펠릿화를 설명한다.↩
-
Maillefer, 전선 및 케이블 절연과 외피용 압출기, provides a current manufacturer reference for screw-based extruders used across cable insulation and sheathing applications; final screw and line selection remains application-specific. ↩
