PRODUCTION LINE PREVIEW
참조 구성SHIELDED CONSTRUCTION REVIEW
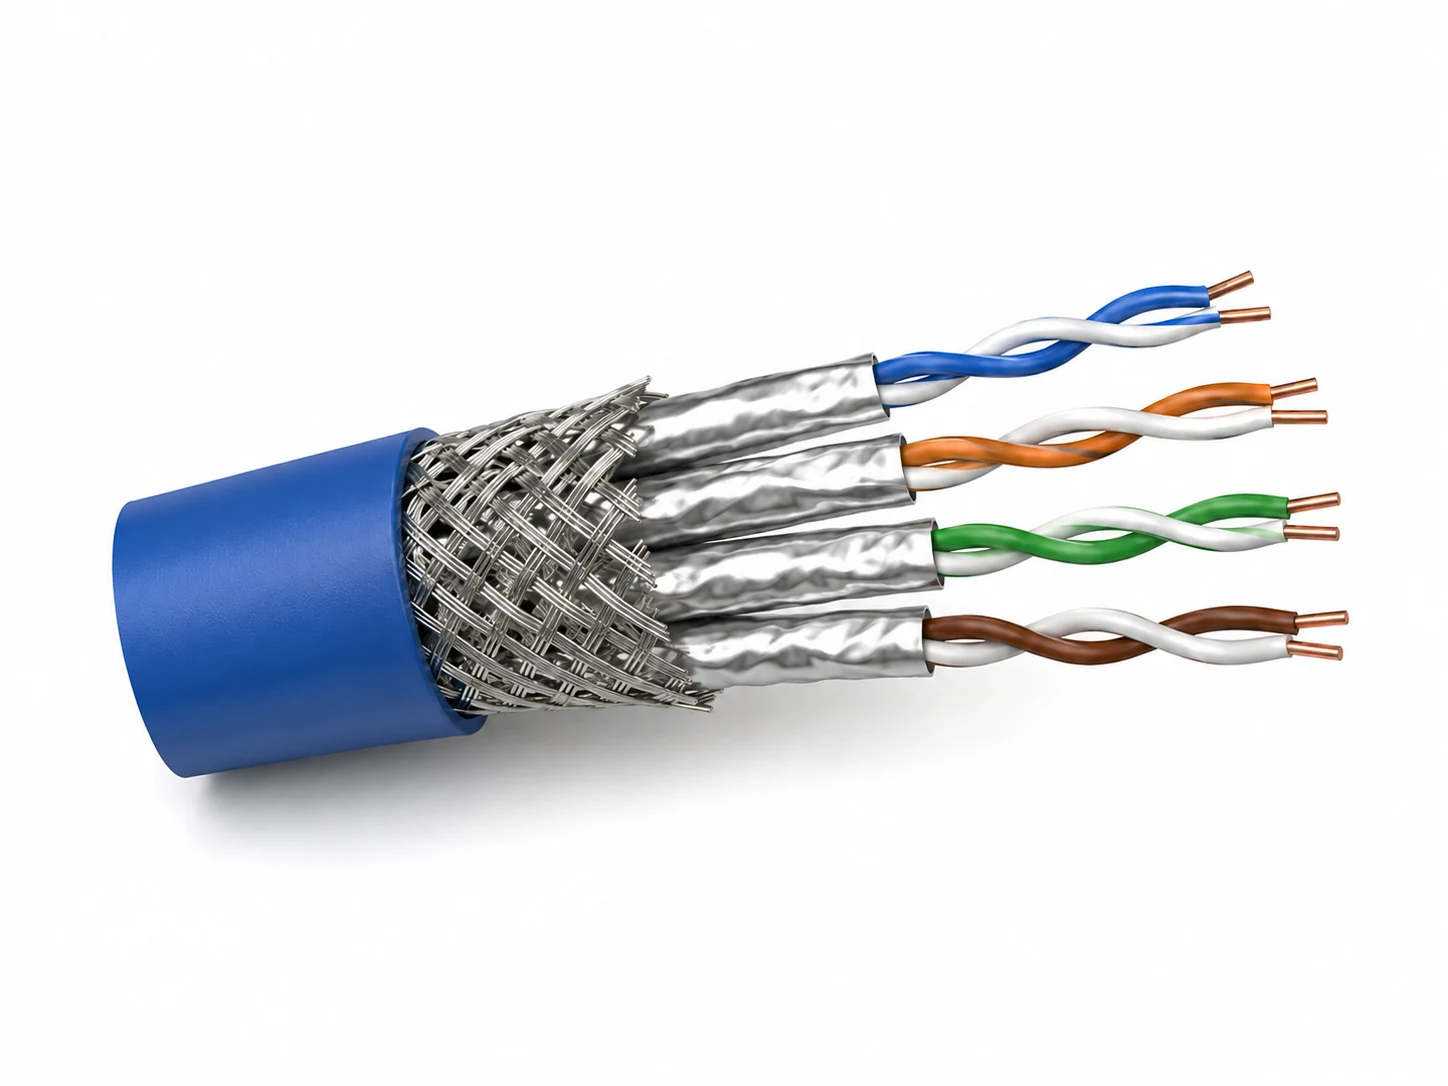
4 PAIRS · FOIL & BRAID S/FTP shown as a 3D reference render, not CAD or an approved project drawing. Confirm the foil path and final shielding.
제품 및 생산
제작하려는 케이블부터 시작하세요.
HONGKAI 기계 장비의 교체 부품.
공장을 완전히 계획하고 계십니까?
제품, 생산 라인 및 자재 요구사항을 연결하세요.
통합 공장 솔루션
완전한 케이블 라인, 자재, 레이아웃 및 시운전 지원.
케이블 제조, MPO 조립 및 최종 광학 테스트.
베이스 케이블, 커넥터 어셈블리, 폴리싱 및 출하.
네트워크 케이블용 장비 선정 및 공정 계획.
투자하기 전에 신중한 결정을 내리세요.
투자 입력 요소를 이해하세요
공정 연구를 검토하세요
트리플 트위스트와 더블 트위스트를 비교하세요
귀하의 제품이 출발점입니다.
해당 장비와 자재, 그리고 이를 중심으로 공장을 계획하세요.
01SELECTED PRODUCTION LINE
절연, 발포, 테이핑 및 브레이딩 공정을 포함한 프로젝트 기반 구성입니다.
PRODUCTION LINE PREVIEW
참조 구성SHIELDED CONSTRUCTION REVIEW
4 PAIRS · FOIL & BRAID S/FTP shown as a 3D reference render, not CAD or an approved project drawing. Confirm the foil path and final shielding.
Plan a CAT6A or CAT7 LAN cable project around the supplied eight-family equipment schedule. Review solid insulation and physical foaming, separator production, back-twist pairing, cabling and taping, metal braiding, sheathing and coiling. The final route follows your cable drawing and acceptance plan.
02CABLE SPECIFICATION
기계 선택은 필요한 케이블의 결과이지, 출발점이 아니다.
03CABLE STRUCTURE
레이어를 선택하여 기능, 제조 단계 및 제어 책임을 확인합니다.
SELECTED LAYER · 03
이것은 근접 간섭 제어의 핵심 공정 관계이며, 최종 값은 승인된 케이블 설계를 따릅니다.
04MANUFACTURING PROCESS
Seven process decisions connect the source equipment schedule to the finished cable. Separator and shielding stages follow the selected design.
3D reference render
Choose between the 60+35 insulation route and the physical-foaming tandem route after confirming the dielectric system. The source foaming details discuss FEP; a different compound needs qualification.
05PERFORMANCE CONTROL MAP
Confirm the CAT6A or CAT7 test basis and cable drawing before setting process controls.
Conductor dimensions, concentricity and the approved solid or foamed insulation structure
Pair-specific lay, back-twist settings, tension and geometry repeatability
조립 장력, 승인된 분리기 위치, 호일 경로 및 브레이드 피복률
자켓 두께, 냉각 및 표면 품질
Taping and braiding modules do not by themselves establish an S/FTP construction. Confirm each pair-foil path, overall shield, drain wire where specified and the final electrical acceptance tests.
06REQUIRED EQUIPMENT
The quantities below reproduce the supplied project schedule. They are a reference allocation, not a fixed minimum for every CAT6A or CAT7 factory.
도체 준비, 압출, 냉각 및 온라인 모니터링을 통해 색상 식별 절연 코어를 생산합니다.
1 set · source allocation케이블 드로잉 공정에서 필요할 경우, 별도의 상류 재료 스트림으로 플라스틱 십자형 분리기를 압출합니다.
1 set · source allocation문서화된 발포 공정에서 드로잉, 어닐링, 절연 압출 및 질소 주입을 결합합니다.
1 set · source allocationPairs the insulated conductors with back-twist payoff and controlled tension before four-pair assembly.
8 sets · source allocationAssembles the four pairs. The documented package includes pair-to-pair active taping, centre wrapping and side wrapping.
2 sets · source allocationApplies a metallic braid around the assembled core when an overall braided screen is specified.
10 sets · source allocationApplies the approved jacket to the assembled cable core, then cools, checks and takes up the finished cable.
1 set · source allocationWinds finished network cable into the agreed coil format for subsequent packing.
1 set · source allocation3D reference render
SELECTED MODULE · 01PROCESS-TO-EQUIPMENT MAPPING
도체 준비, 압출, 냉각 및 온라인 모니터링을 통해 색상 식별 절연 코어를 생산합니다.
3D reference render · final equipment and construction subject to project approval.
| 장비 | 수량 | Source speed entry | Specification pages |
|---|---|---|---|
| 60+35 High-Speed Insulation Line | 1세트 | 800–1,000 m/min · schedule reference | 3–11 |
| HK-50 Cross-Separator Line | 1세트 | 120 / 450 m/min · conflicting source entries | 12–18 |
| 물리적 발포 탠덤 라인 | 1세트 | Foaming 500; core wire 1,000; design 1,200 m/min · p.28 | 19–29 |
| 500 Back-Twist Pairing System | 8세트 | 33–65 m/min · schedule reference | 30–32 |
| 800 Cantilever Cabling & Taping | 2세트 | 60 m/min schedule; 15–118 m/min detailed range | 33–35 |
| 24-Carrier Metal Braiding Machine | 10 sets | 5 m/min schedule; 329 m/h detailed reference | 36 |
| 80 Outer-Sheathing Line | 1세트 | 120 m/min schedule; 100 m/min detailed line rating | 37–44 |
| 500 LAN Cable Coiling Machine | 1세트 | 150 m/min schedule; 120 m/min in both detailed alternatives | 45–50 |
Source: Cat6/6E/7 Production Line Full Project, 50 pages; page 2 contains the allocation / rate schedule. Its 6E title is not CAT6A certification. Machine design speeds, operating modes and whole-factory output are different measures. Resolve the separator, sheathing and winding rate differences before quotation.
07CONFIGURATION OPTIONS
소스 프로젝트를 참조로 사용한 후, CAT6A 또는 CAT7 케이블에 적합한 경로를 선택하세요.
SOURCE PROJECT CONFIGURATION
Request a project quotation after confirming the cable drawing, equipment allocation, testing scope and commercial terms.
08FUTURE EXPANSION
Plan the intended CAT6A / CAT7 constructions first. Changes to insulation, pair shielding or braid construction need a fresh tooling, material and capacity review.
Reserve space for the approved solid or foamed insulation route, separator handling, taping and braiding requirements.
압출, 쌍선 비틀기, 케이블링, 브레이딩 및 권취 공정 간의 릴 버퍼, 접근성 및 자재 흐름을 계획합니다.
Confirm power, cooling, air, ventilation and control interfaces against the selected compounds and machine scope.
09SELECTION GUIDE
장비 스케줄을 시작점으로 사용하십시오. CAT6A/CAT7 경로를 확정하기 전에 이러한 입력 사항을 확인하세요.
Category, conductor, solid or foamed insulation, pair foil, overall shield, separator and jacket requirements
Project test standard, frequency range, limits, shield checks and instrument capability
제품 구성, 배치 크기, 릴 이송, 작업자, 교체 및 포장 형식
명확한 치수, 유틸리티, 환기, 릴 버퍼 공간 및 설치 접근성
10QUALITY & TESTING
승인된 CAT6A/CAT7 구조에 따라 생산 검사 및 완성 케이블 시험을 수행하십시오.
케이블 제조 중 재현성을 보호하는 관리 항목.
직경, 동심도 및 승인된 솔리드 또는 발포 구조
확인된 컴파운드, 공구 및 검사 방법Pair-specific lay, back-twist, tension and geometry
쌍 설정 및 샘플 확인세퍼레이터 위치, 페어-포일 경로, 테이핑, 브레이드 및 지정된 드레인 와이어 점검
Approved drawing and recorded shield construction두께, 완성 직경, 표면 및 마킹
온라인 및 최종 시각/치수 기록11KNOWLEDGE & RISK CONTROL
Resolve material, shielding and capacity assumptions before approving the equipment configuration.
Core-wire, foaming and design speeds describe different conditions. None is a guaranteed output for the complete production route.
The listed taping functions do not yet confirm four independent pair-foil paths. Match the actual foil route to the approved cable drawing.
Eight pair-twisting units and ten braiding units are schedule quantities. Batch sizes, reel buffers, changeovers and tested output still require capacity planning.
12DELIVERY BOUNDARIES
Confirm models, quantities, tooling, interfaces and test responsibilities in the final technical proposal.
The agreed machinery scope must identify each extrusion, twisting, cabling, taping, braiding and coiling module.
Confirm separator tooling, foam-system interfaces, foil handling, braid setup, reel transfers and selected peripherals.
Identify specialist instruments, test services and customer-supplied utilities separately. A machine list is not a complete acceptance package.
13 PROCESS VIDEO REFERENCES
These HONGKAI videos were selected for CAT6A / CAT7-relevant operations. They remain process references rather than proof that the exact source-schedule units, materials or finished-cable acceptance have been confirmed.
These five references do not cover or verify all eight equipment families. No confirmed video has been assigned to the cross separator, the source-schedule physical-foaming line or the 24-carrier metal braider. No video here establishes the new project's acceptance result, output or guaranteed cable performance. Reference 03 illustrates pair-to-pair taping but does not confirm the complete four-pair shielding path.
14 PROJECT REFERENCE REVIEW
For a CAT6A / CAT7 project, compare the actual insulation, pair-foil and overall-shield construction. A similar machine or category label alone is not a matching acceptance reference.
카테고리, 솔리드/포밍 절연체, 분리막, 개별 쌍 호일, 전체 차폐층 및 재킷이 식별됩니다.
Match all eight scheduled equipment families, quantities, foil paths, tooling and included services.
고객 신원, 국가 및 프로젝트 미디어는 허가 시에만 공개됩니다.
Category, test method, frequency range, limits, trial conditions and results are supported by project records.
The supplied schedule is headed 6E. It is an equipment-planning reference, not evidence of CAT6A / CAT7 compliance. Confirm the project drawing and acceptance basis separately.
14B EXISTING CAT6 PROJECT EXPERIENCE
These customer-approved comments describe existing CAT6 projects. They are retained as HONGKAI planning experience, not reviews or acceptance evidence for CAT6A / CAT7 equipment.
For our CAT6 project, HONGKAI explained how conductor insulation, pair-specific twisting and cabling settings relate to the agreed electrical test requirements. This made the proposed equipment scope easier to understand.
The CAT6 planning discussion covered the workshop layout, utility interfaces and separator handling where required by the cable drawing. That gave our team a clearer basis for reviewing the proposed production route.
We valued the clear distinction between a CAT6 U/UTP route and the additional overall foil and drain-wire handling for F/UTP. The proposal discussion also identified which testing and supply-scope details needed confirmation.
15 자주하는 질문
프로젝트별 답변이 필요하신가요? 아래에 케이블 사양과 공장 조건을 보내주세요.
아니요. 제공된 스케줄은 6E로 표시되어 있습니다. CAT6A/CAT7 적합성 확보를 위해서는 여전히 승인된 케이블 도면, 확인된 절연 및 차폐 경로, 그리고 프로젝트별 전기적 승인 계획이 필요합니다.
Not by itself. The schedule includes taping and metal braiding, but four independent pair-foil paths are not yet confirmed. Check each pair wrap and the overall shield against the intended cable construction.
The supplied description names physically foamed FEP. Do not substitute PE or another compound without reviewing the material system, tooling and process conditions. Confirm the insulation route for each intended product.
The schedule lists eight equipment families, including eight pair-twisting units, two cabling/taping units and ten braiding units. These quantities do not prove balanced output. Confirm batch routing, reel transfers, changeovers and capacity against the product mix.
의도된 카테고리, 케이블 도면, 도체 및 절연 세부사항, 분리막, 개별 쌍 호일 및 전체 차폐 구조, 재킷 및 내화 요구사항, 목표 생산량, 작업장 설비 및 인수 시험을 제공하십시오.
아니요. 연속성 및 식별은 기본 점검 사항입니다. 수용 기준을 정의하기 전에 CAT6A 또는 CAT7 테스트 표준, 주파수 범위, 한계값, 차폐 검사 및 측정 장비의 성능을 사전에 합의해야 합니다.
The proposal should identify HONGKAI-manufactured modules, integrated specialist items and customer-supplied interfaces separately. Final test instruments, laboratory checks and responsibilities are agreed project by project.
No. Design speed, core-wire speed and foaming speed describe different conditions. Usable output for each stage and the complete route must be confirmed against the materials, cable construction, configuration and acceptance conditions.
16 PROJECT ENQUIRY
Start with the intended CAT6A / CAT7 drawing, insulation material, pair-foil and overall-shield construction. Add your factory conditions and acceptance requirements so HONGKAI can review the equipment scope.
이 문의는 초기 기술 논의를 지원합니다. 견적, 성능 보증, 확정된 장비 목록, 최종 공급 범위, 납기 일정 또는 수락 약속이 아닙니다.