• 에 대한
    • PRODUCTS & PRODUCTION

      다음 생산 단계를 찾으세요.

      Production lines

      제작하려는 케이블부터 시작하세요.

      광케이블 라인

      광케이블 제조 장비

      LAN cable lines

      꼬임쌍 케이블용 장비

      전기 케이블 기계

      절연 전선 및 케이블용 기계장치

      예비 부품 및 지원

      HONGKAI 기계 장비의 교체 부품.

      스페어 부품 둘러보기

      생산 라인별 부품 살펴보기

      귀하의 부품 식별

      사진, 명판 및 부품 번호를 확인하세요.

      부품 견적 요청하기

      기계 세부 사양, 사진 및 수량을 보내주십시오.

      케이블 및 재료

      케이블 구조와 입력을 살펴보세요.

      광섬유 케이블

      광섬유 케이블 유형 찾아보기

      원자재

      광케이블 생산용 재료

  • 블로그
  • 연락하다

제어 케이블 생산 라인

What is a control cable production line? It prepares the specified copper conductors, extrudes and identifies the insulated cores, lays them up and applies an outer sheath. Add a screen only when the cable design requires it, then verify core identity, continuity and the specified electrical properties.

Cable designation
Seven-core PVC reference
도체 재질
Copper · class to confirm
도체 공정
Insulate → Identify → Lay up → Sheath
Final configuration
Confirmed against the approved cable design
Cable structure preview 참조 케이블
Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustration Structure reference. Final design pending. Cable structure below Review materials and construction
What the client selected Control Cable · Seven-core PVC reference Seven-core unshielded PVC illustration. Confirm conductor class, core count and identification, any screen construction, sheath and packing format.
02 Cable definition

Define the Control Cable Before Selecting Equipment

This reference shows seven insulated copper cores inside an outer sheath. It has no depicted metallic screen or armour. Confirm the actual core count, identification and any optional screen before defining the process.
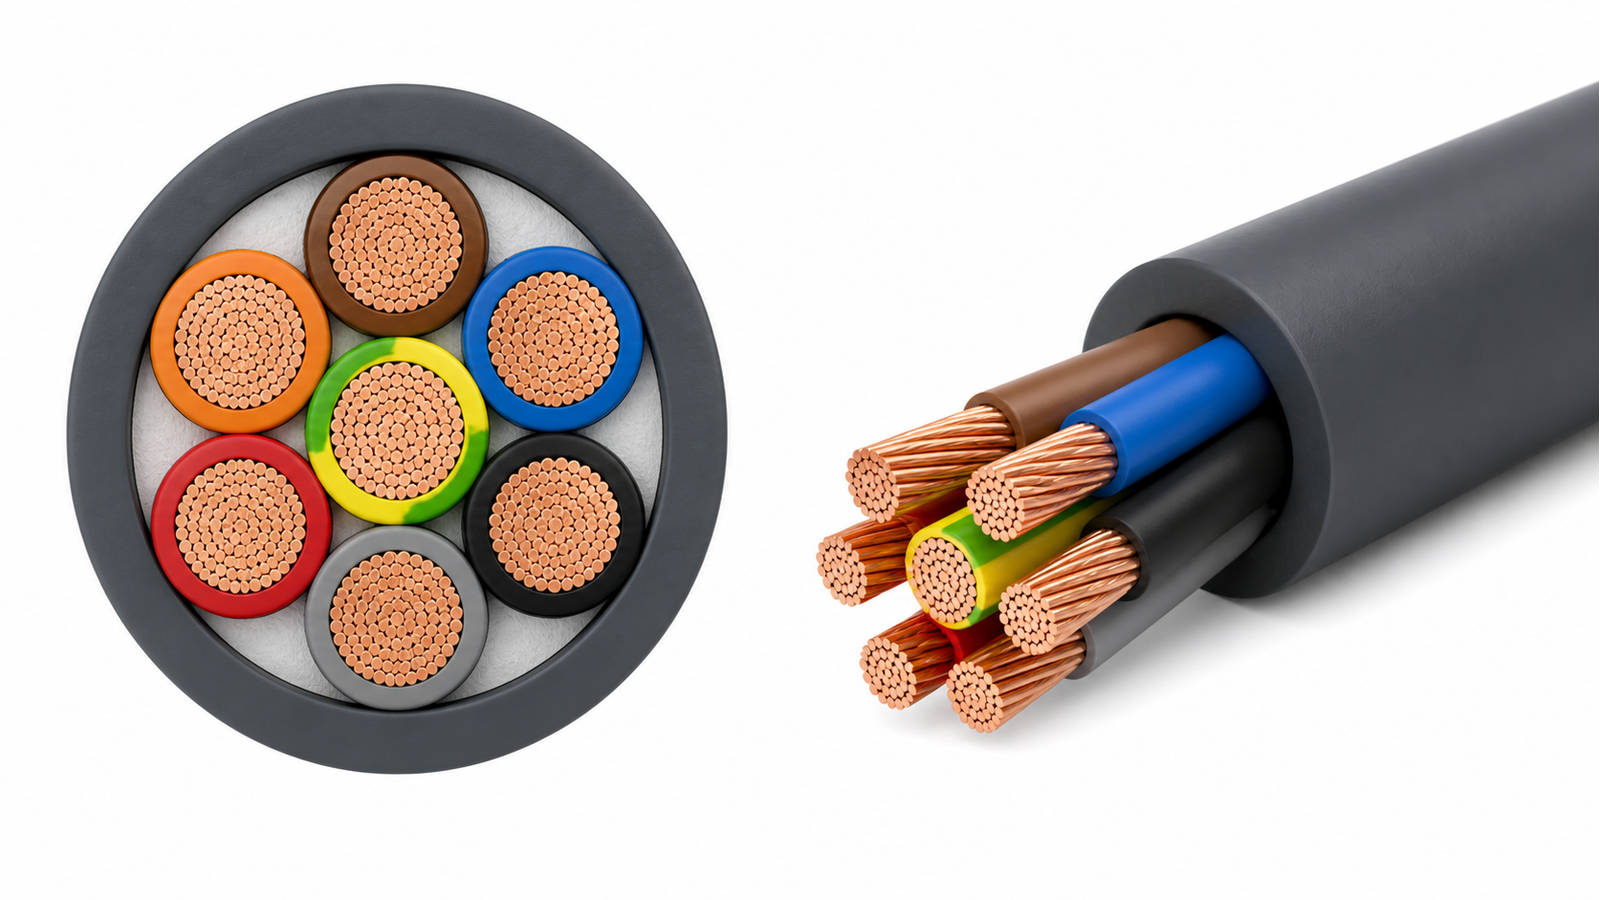
Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustration
control cable construction reference The artwork does not confirm a customer sample, standard, material grade, dimensions or production range.
Current project definition

Known inputs and open confirmations

케이블 패밀리
Multi-core copper control cable
Reference construction
Seven-core, unshielded PVC illustration
Conductor class
Copper; solid, stranded or flexible construction as specified
Nominal area / wire construction
Area per core, individual-wire size, count and finished conductor diameter
Insulated-core count
Seven shown; actual core count and any mixed sizes to confirm
Core identification
Approved colours or numbers, marking method and protective-core identification
절연
Compound grade, wall, core diameter and specified test conditions
코어 조립
Sequence, lay, fillers / binder, tension and bundle diameter
Screen option
참조 자료에 해당 사항 없음; 포일, 브레이드 또는 복합 설계는 검토 필요
Screen details if specified
Material, coverage / overlap, wire or tape sizes, drain wire and separation layers
외부 외피
PVC reference; approved compound, wall, finished diameter and marking
Service conditions
Voltage, fixed or moving duty, bend limits and environment from the design
포장
Coil, reel or drum geometry, length and maximum loaded mass
수락
Core identity / continuity, specified electrical and dimensional tests
Core identity must survive laying-up and finishing.Specify conductor construction separately from cable core count. Agree the colour or numbering scheme, core sequence and protective-core requirements in the cable design. A screen is an additional construction layer; it is not armour.
03 예비 공정 경로

Match the Route to the Cable Construction

Choose the incoming material, then state whether a screen is required. The reference cable is unshielded. A screened design adds a dedicated review of the screen application stage before the outer sheath.

Prepare copper wires / form conductors → Insulate and identify cores → Core checks → Lay up identified cores → Outer sheath → Cool, test and pack Upstream stages depend on conductor construction and incoming material. Solid conductors bypass conductor formation.
Typical process / not a fixed layout

Screen decision point: the default route is unshielded. A specified foil, braid or combined screen needs its own materials, application equipment, coverage requirements and checks. The seven-core illustration does not show a screen. Core identification and continuity must remain traceable through cabling and finishing.

Copper conductor bunching machine, existing 3D reference
Stage 02 / Before insulation / stranded design

Conductor Formation

Bunch or strand the copper wires to the specified conductor class and area. Solid conductors bypass this operation.

입력
허용된 동선 및 승인된 도체 구조
출력
Accepted bare conductor on a compatible reel
장비 공급처
Conductor formation equipment; category checked against HONGKAI catalogue p. 47; 3D reference
Confirm
Wire size and count, conductor class, lay, resistance, tension and reel format
04 필요한 단계별 장비

Review the Equipment Categories for This Route

Match each equipment function to the cable design. The 3D illustrations show equipment categories and process arrangements. The final model, operating range and interfaces are confirmed for the project.
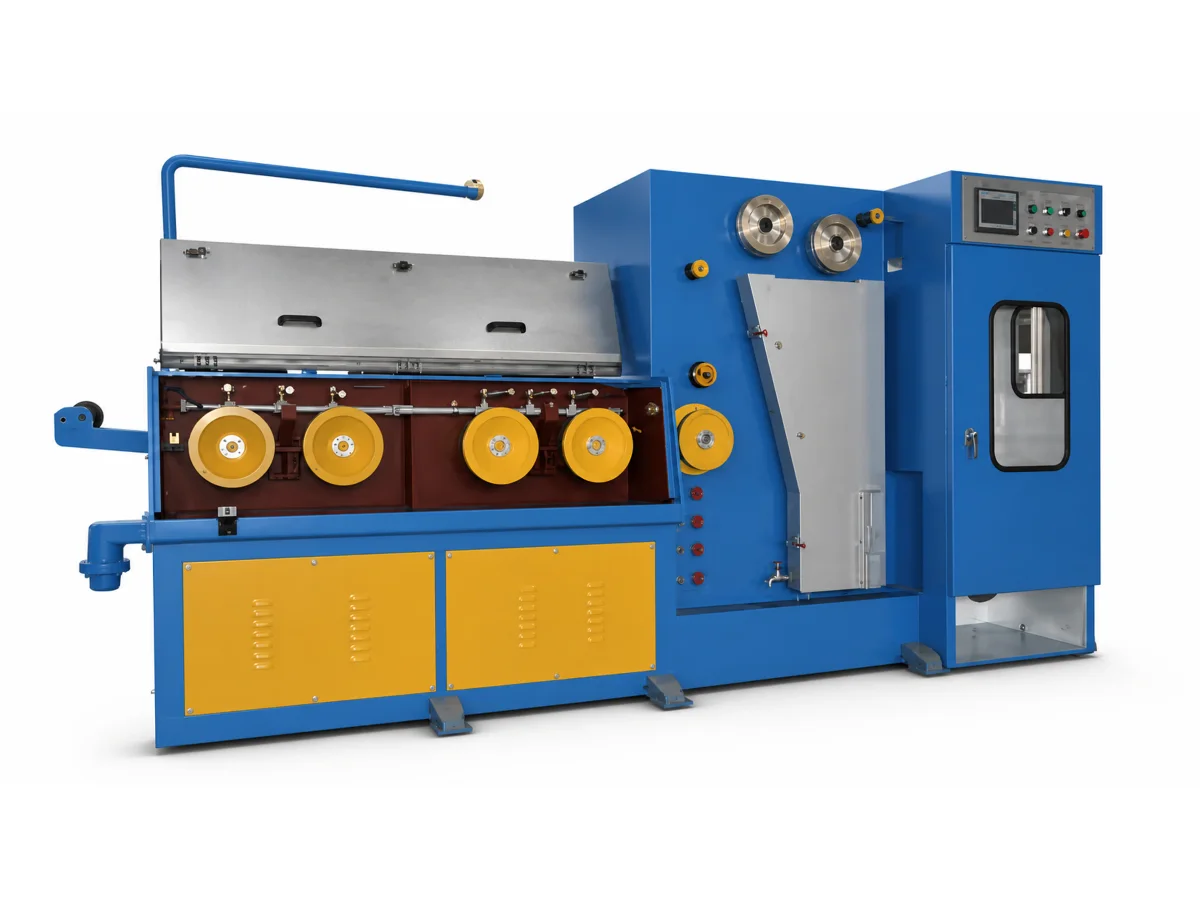
Wire drawing machine, existing 3D equipment reference3D equipment reference; final size and configuration to confirm
01 / Equipment configuration

와이어 준비

Prepare copper wire to the required diameter and material condition, only where this upstream stage is needed.

Route status
Upstream / if required
Source boundary
Wire drawing equipment; category checked against HONGKAI catalogue p. 45; 3D reference
구성
Copper grade, incoming size, wire diameter, condition, reel and inspection requirements
Key input
Specified incoming copper rod / wire

Copper grade, incoming size, wire diameter, condition, reel and inspection requirements

05 Manufacturing and integration

Keep Every Equipment Source and Responsibility Explicit

A coordinated production-line project does not mean one factory manufactures every machine. Each source and interface is defined in the approved proposal.

Control Cable, one coordinated project interface

Equipment source, contracting entity, integration boundary and service responsibility stay item-specific.

Proposal-defined scope
01 / HONGKAI manufacturing scope

HONGKAI에서 제조

Core-insulation and outer-sheathing equipment only where expressly identified as HONGKAI-manufactured in the confirmed proposal.

  • Insulation and sheathing equipment identified in the proposal
  • Mechanical assembly and electrical-control scope only as defined for each identified item
  • Factory inspection or testing only where stated in the approved proposal
Final configuration and responsibility, To be confirmed
02 / Specialist manufacturing scope

전문 제조업체로부터 통합

Conductor formation, core laying-up and any specified foil or braid screening system. Sources and interfaces are defined for each item.

  • Conductor formation matched to the specified copper class
  • Core laying-up with controlled tension and identity management
  • Screen application only where required by the approved design
  • 제안서에 명시된 소스 및 계약 경계
Equipment source and scope, To be confirmed
03 / Supporting systems

보조 장비 및 프로젝트 인터페이스

Cooling, inspection, core identification, any required screen checks, take-up, packing and agreed utilities.

  • Exact functions and equipment source remain project-specific
  • Customer-side utilities and interface responsibilities
  • Installation, commissioning and training scope if agreed
Any HONGKAI-configured or supplied supporting items: To be confirmed in the proposal
06 공장 계획 입력

Plan the Factory Around the Confirmed Line Scope

Select only the information you already have. This checklist records readiness for review and does not save or submit project data.

07 Quality checkpoints

Keep Core Identity Traceable Through Final Testing

Agree the inspection plan before equipment selection. Equipment illustrations show the named device only; finished-cable acceptance requires the agreed test methods and records.

Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustrationConductor acceptance
Conductor acceptance

Check Conductors and Core Identity

Verify conductor construction and resistance, then maintain the approved colour or numbering scheme and core sequence through each process.

Wire count inside one conductor is not the number of insulated cores. The 3D cable is a structure illustration, not a test sample.
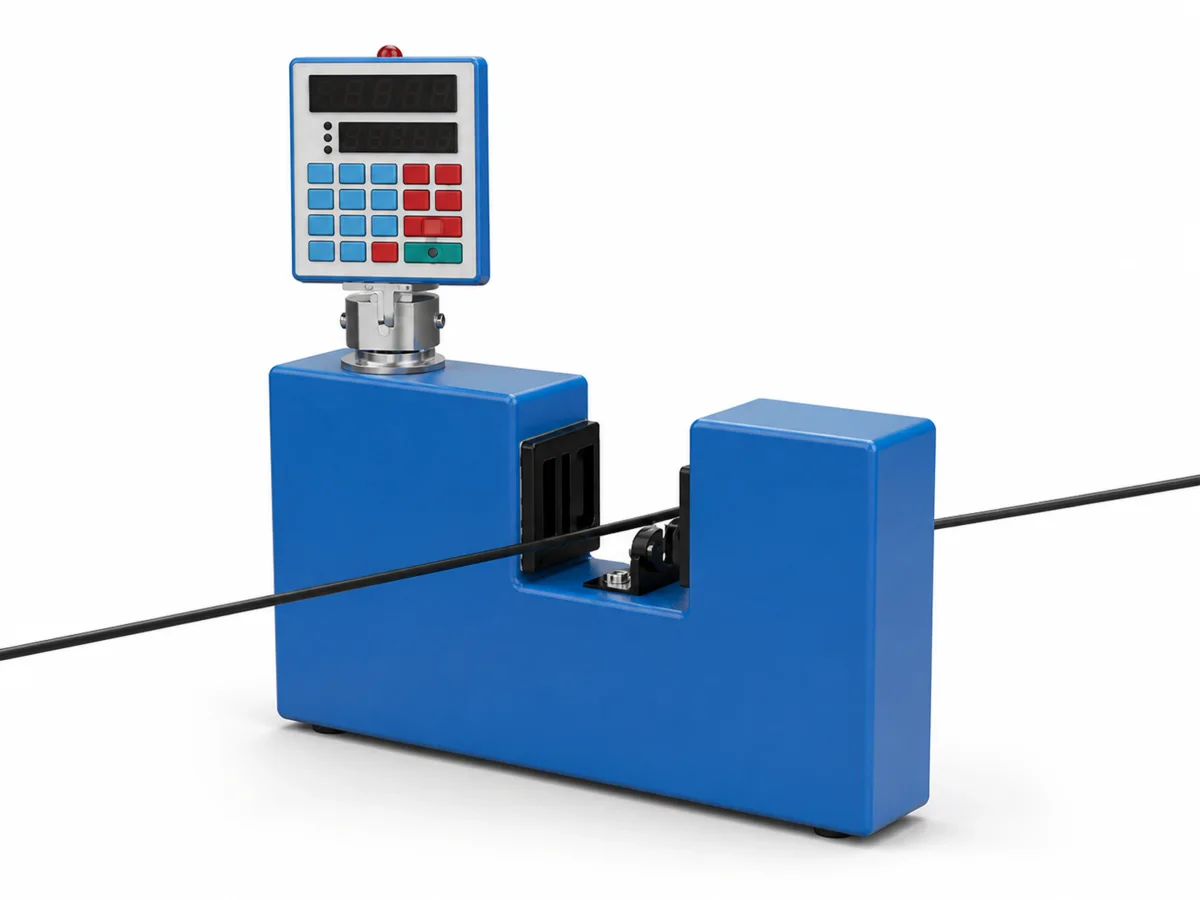
Laser outside-diameter gauge, existing 3D equipment referenceDimensional control
Dimensional control

Measure Diameter; Verify the Wall

Measure insulated-core and finished-cable diameters. Verify core insulation and outer-sheath wall thickness separately by the approved measurement method.

A laser outside-diameter gauge alone cannot establish minimum wall thickness. The acceptance method and tolerances must be defined.
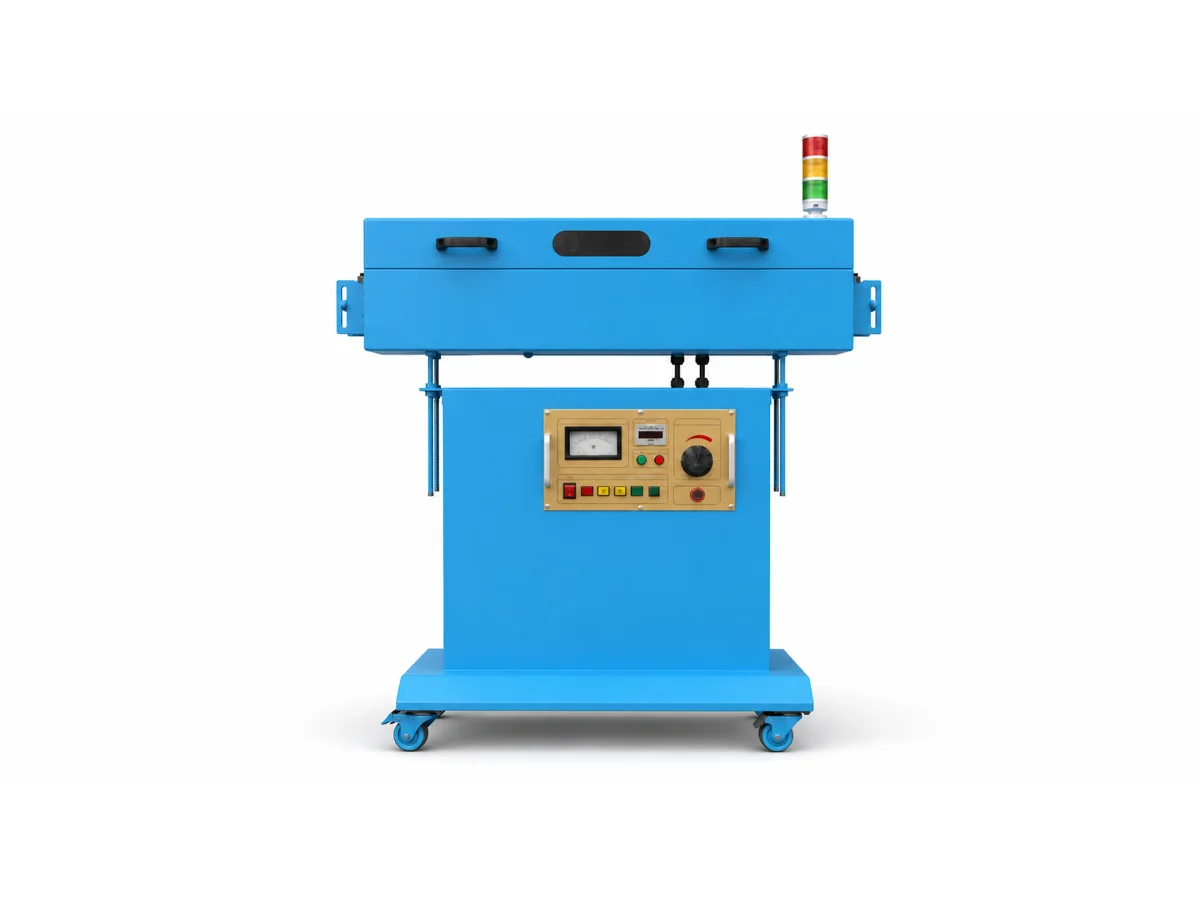
Insulated-core spark tester, existing 3D equipment referenceIn-line electrical check
In-line electrical check

Inspect the Dry Insulation

Cool and dry each insulated core before its specified spark test. Record faults and keep accepted core reels identifiable before cabling.

Core spark testing does not replace finished-cable electrical tests. Any sheath integrity test needs its own approved method and suitable electrical arrangement.
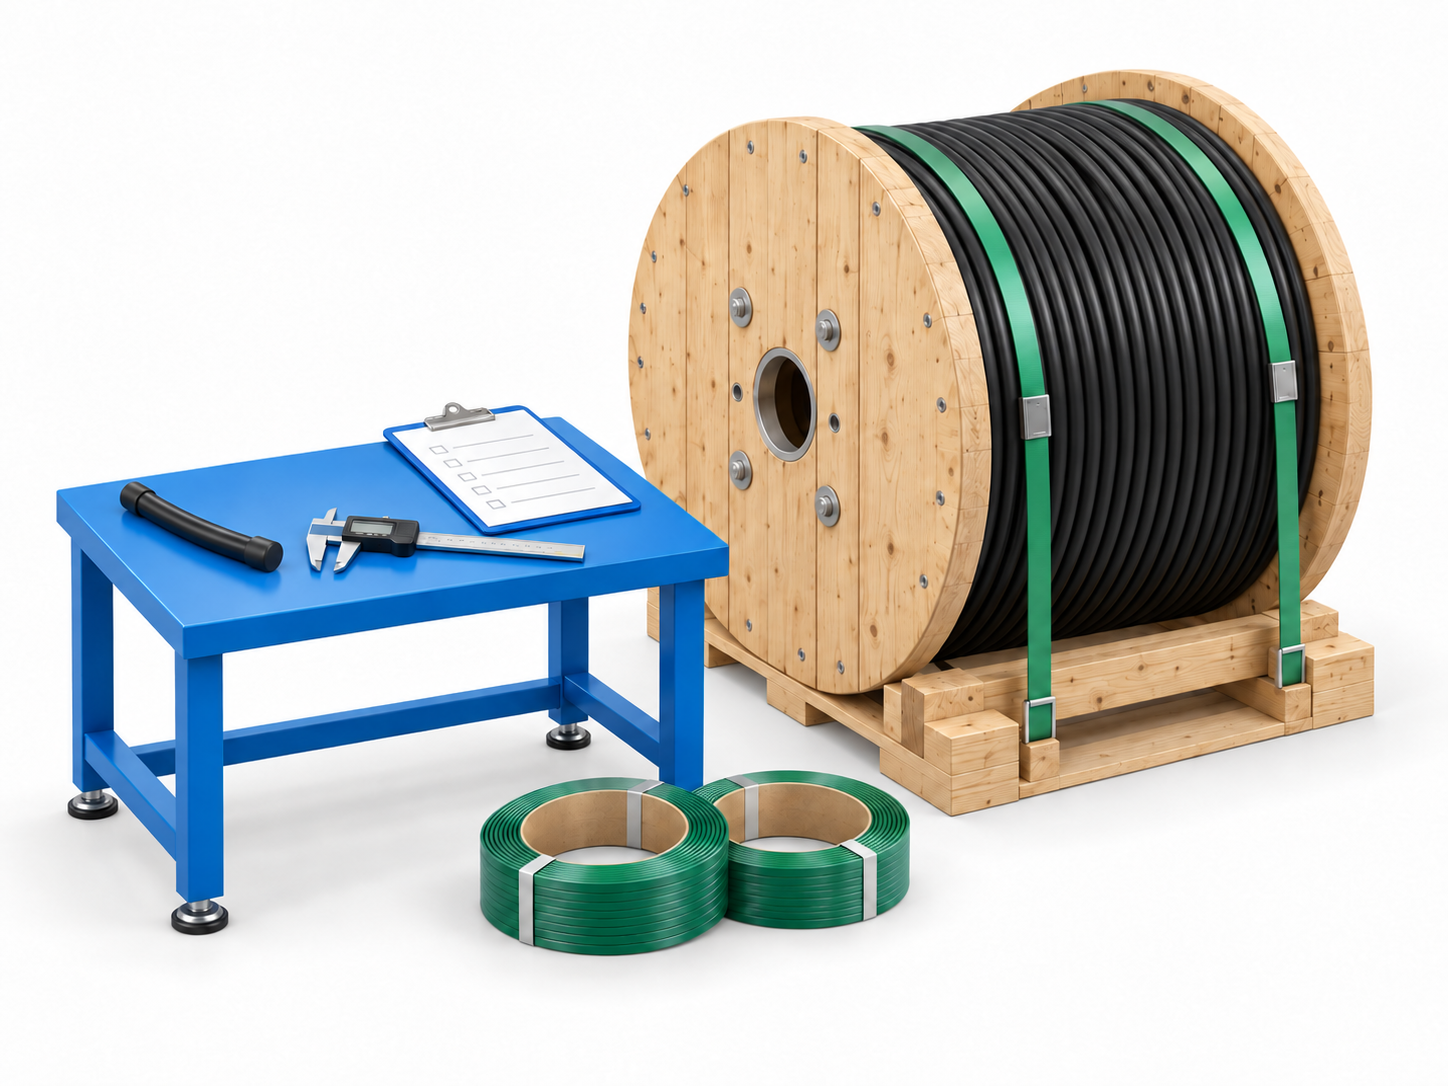
3D workflow illustration of a finished cable drum, dimensional inspection tools and packing recordsFinished-product release
Finished-product release

Verify Continuity and Packing

Confirm core identification and continuity, specified electrical and dimensional tests, and screen checks only where required. Verify cable marking, length and the agreed packing format.

Release the finished cable only against the agreed test results, identification, length and packing records.
Keep illustration and evidence separate. Add actual trial records, sample measurements and project acceptance documents once available. No performance or certification is inferred from a render.
Project records required
08 자주하는 질문

Clarify the Route Before Requesting a Quote

These answers explain the decision path. They do not replace an approved cable design, technical solution, quotation or project proposal.

What does a control cable production line include?

The preliminary route includes copper-wire preparation and conductor formation where required, core insulation and identification, core checks, laying-up, outer sheathing, cooling and final tests. A screen application stage is added only for a specified screened construction.

Is every control cable screened?

No. The seven-core reference is unshielded. Foil, braid or combined screens belong to a separate approved construction. Select the required screen in the route review and provide its dimensions, material and acceptance requirements.

How are cores identified during production?

Use the colours or numbers specified by the approved cable design. Confirm the marking method, legibility and sequence before laying-up, then verify identification and continuity on the finished cable. The illustration does not establish a universal colour scheme.

Are conductor bunching and core laying-up the same operation?

No. Bunching or stranding forms one bare conductor from individual wires before insulation. Laying-up assembles separately insulated and identified cores. Choose both systems for the actual conductor class, core size, lay and reel format.

Can the same screening equipment apply foil and braid?

Do not assume interchangeability. Foil application needs suitable tape handling and overlap control; braiding uses a different application arrangement and coverage controls. Drain wires, separators and combined screens also require a defined process.

Does a flexible conductor automatically make the cable suitable for continuous movement?

No. Moving duty depends on the complete cable construction, materials, lay, bend conditions and qualification requirements. State fixed installation or the required movement duty before equipment and material selection.

Which checks are required on the finished control cable?

Agree core identification and continuity checks, conductor resistance, specified electrical and insulation tests, dimensions and marking. Add screen continuity or other screen-related acceptance only where the design requires it, then verify length and packing.

What information is needed to select the equipment?

Provide conductor area and class, wire construction, core count and identity, insulation and sheath compounds and walls, any screen specification, output mix, finished diameter and packing format. Models, speeds and supply responsibilities are confirmed in the proposal.

09 Control Cable project enquiry

Plan Your Control Cable Production Line

Share conductor class and size, core count and identification, insulation and sheath. If screening is required, include the foil or braid construction, drain wire and acceptance requirements.

Route currently on this page

  • 케이블 패밀리제어 케이블
  • Current route reviewPrepare copper wires / form conductors → Insulate and identify cores → Core checks → Lay up identified cores → Outer sheath → Cool, test and pack
  • Conductor inputsCopper class and size, core identity, optional screen design and sheath
  • 완성된 코어 수Seven cores in the artwork; actual count and identification to confirm.

Optional. Review the copied context before sending.

An enquiry requests a project-scope review. It does not confirm equipment configuration, material compatibility, price, delivery schedule, output, factory acceptance or project result.

Compare all cable solutions

Control Cable Project Enquiry

Fields marked * are required. Technical inputs may remain to be confirmed.

The dedicated enquiry form has not been connected yet. Please contact HONGKAI through the 프로젝트 문의 페이지.

Your contact details

기술 후속 조치를 받을 사람은 누구입니까?
Include country code, if provided.

Conductor and cable construction

Define each conductor separately from cable core count; include core identification and any required screen.
Applicable product standard and rated voltage from the approved design.
Copper conductor class, wire construction and finished dimensions.
Area in mm², not the sum of all cores.
For stranded conductors, wire dimensions by layer if needed.
For stranded conductors; state solid where applicable.
절연 전 외경(mm).
Number of separately insulated cores in the finished cable.
Colour or number scheme, marking method, sequence and protective core as specified.
Approved insulation compound, grade and nominal / minimum wall.
Target and tolerance in mm.
Lay length, direction and bundle OD before sheathing, if known.
Only where specified by the cable drawing.
Specified sheath compound and nominal / minimum wall.
Target and tolerance after sheathing, in mm.
None, foil, braid or combined; material, coverage / overlap, drain wire and separators if required.
Flange and barrel diameter, width, bore, cable length and maximum loaded mass.
State the installation or movement conditions and required cable / screen tests.

Project requirements

Final range, output and equipment interfaces require technical review.
Cable size, quantity, unit, working hours and product mix.
파일을 드래그 앤 드롭하거나, 업로드할 파일 선택 최대 3 파일을 업로드할 수 있습니다.
Optional: PDF, JPG, JPEG or PNG. Up to 3 files, 10 MB each.
Use Add Viewed Route to Form, then review or edit the copied context.

견적을 요청하세요

우리는 24시간 이내에 당신에게 대답할 것입니다!!!