• بيت
  • عن
    • PRODUCTS & PRODUCTION

      اعثر على خطوتك الإنتاجية التالية.

      خطوط الإنتاج

      ابدأ بالكابل الذي تريد تصنيعه.

      خطوط كابلات الألياف البصرية

      معدات تصنيع الكابلات الضوئية

      خطوط كابلات LAN

      معداتات كابل الزوج الملتوي

      ماكينات الكابلات الكهربائية

      ماكينات الأسلاك والكابلات المعزولة

      قطع الغيار والدعم

      قطع غيار لآلات HONGKAI.

      تصفح قطع الغيار

      استكشف الأجزاء حسب خط الإنتاج

      تحديد قطعتك

      تحقق من الصور واللوحات التعريفية وأرقام القطع

      طلب عرض أسعار للقطع

      أرسل تفاصيل الماكينة والصور والكمية

      الكابل والمواد

      استكشف هياكل الكابلات والمدخلات.

      كابلات الألياف البصرية

      تصفح أنواع كابلات الألياف البصرية

      مواد خام

      مواد إنتاج الكابلات الضوئية

  • مدونة
  • اتصال

خط إنتاج كابلات التحكم

What is a control cable production line? It prepares the specified copper conductors, extrudes and identifies the insulated cores, lays them up and applies an outer sheath. Add a screen only when the cable design requires it, then verify core identity, continuity and the specified electrical properties.

Cable designation
Seven-core PVC reference
مادة الموصل
Copper · class to confirm
مسار الموصل
Insulate → Identify → Lay up → Sheath
Final configuration
Confirmed against the approved cable design
Cable structure preview كابل مرجعي
Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustration Structure reference. Final design pending. Cable structure below Review materials and construction
What the client selected Control Cable · Seven-core PVC reference Seven-core unshielded PVC illustration. Confirm conductor class, core count and identification, any screen construction, sheath and packing format.
02 Cable definition

Define the Control Cable Before Selecting Equipment

This reference shows seven insulated copper cores inside an outer sheath. It has no depicted metallic screen or armour. Confirm the actual core count, identification and any optional screen before defining the process.
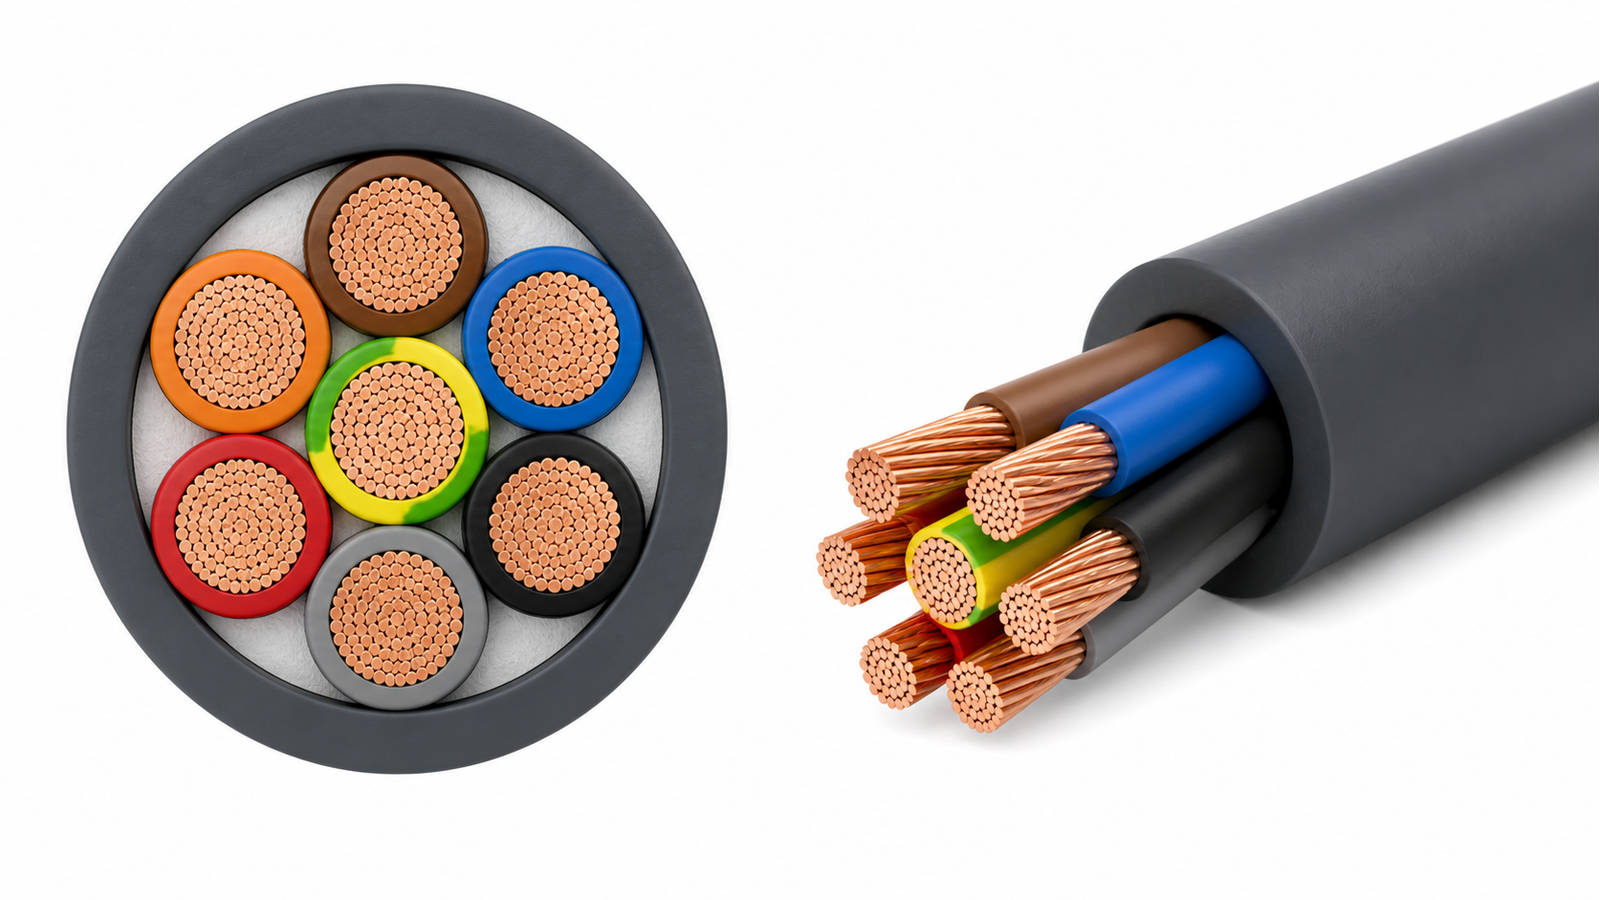
Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustration
control cable construction reference The artwork does not confirm a customer sample, standard, material grade, dimensions or production range.
Current project definition

Known inputs and open confirmations

عائلة الكابلات
Multi-core copper control cable
Reference construction
Seven-core, unshielded PVC illustration
Conductor class
Copper; solid, stranded or flexible construction as specified
Nominal area / wire construction
Area per core, individual-wire size, count and finished conductor diameter
Insulated-core count
Seven shown; actual core count and any mixed sizes to confirm
Core identification
Approved colours or numbers, marking method and protective-core identification
عازل
Compound grade, wall, core diameter and specified test conditions
تجميع النواة
Sequence, lay, fillers / binder, tension and bundle diameter
Screen option
None in the reference; foil, braid or a combined design requires review
Screen details if specified
Material, coverage / overlap, wire or tape sizes, drain wire and separation layers
غلاف خارجي
مرجع PVC؛ مركب معتمد، جدار، قطر خارجي نهائي وعلامة
Service conditions
Voltage, fixed or moving duty, bend limits and environment from the design
التعبئة
Coil, reel or drum geometry, length and maximum loaded mass
القبول
Core identity / continuity, specified electrical and dimensional tests
Core identity must survive laying-up and finishing.Specify conductor construction separately from cable core count. Agree the colour or numbering scheme, core sequence and protective-core requirements in the cable design. A screen is an additional construction layer; it is not armour.
03 مسار العملية الأولي

Match the Route to the Cable Construction

Choose the incoming material, then state whether a screen is required. The reference cable is unshielded. A screened design adds a dedicated review of the screen application stage before the outer sheath.

Prepare copper wires / form conductors → Insulate and identify cores → Core checks → Lay up identified cores → Outer sheath → Cool, test and pack Upstream stages depend on conductor construction and incoming material. Solid conductors bypass conductor formation.
Typical process / not a fixed layout

Screen decision point: the default route is unshielded. A specified foil, braid or combined screen needs its own materials, application equipment, coverage requirements and checks. The seven-core illustration does not show a screen. Core identification and continuity must remain traceable through cabling and finishing.

Copper conductor bunching machine, existing 3D reference
Stage 02 / Before insulation / stranded design

Conductor Formation

Bunch or strand the copper wires to the specified conductor class and area. Solid conductors bypass this operation.

المدخل
Accepted copper wires and approved conductor construction
المخرج
Accepted bare conductor on a compatible reel
مصدر المعدات
Conductor formation equipment; category checked against HONGKAI catalogue p. 47; 3D reference
Confirm
مقاس السلك وعدد الأسلاك، وفئة الموصل، واللفة، والمقاومة، والشد، وشكل البكرة
04 المعدات حسب المرحلة المطلوبة

Review the Equipment Categories for This Route

Match each equipment function to the cable design. The 3D illustrations show equipment categories and process arrangements. The final model, operating range and interfaces are confirmed for the project.
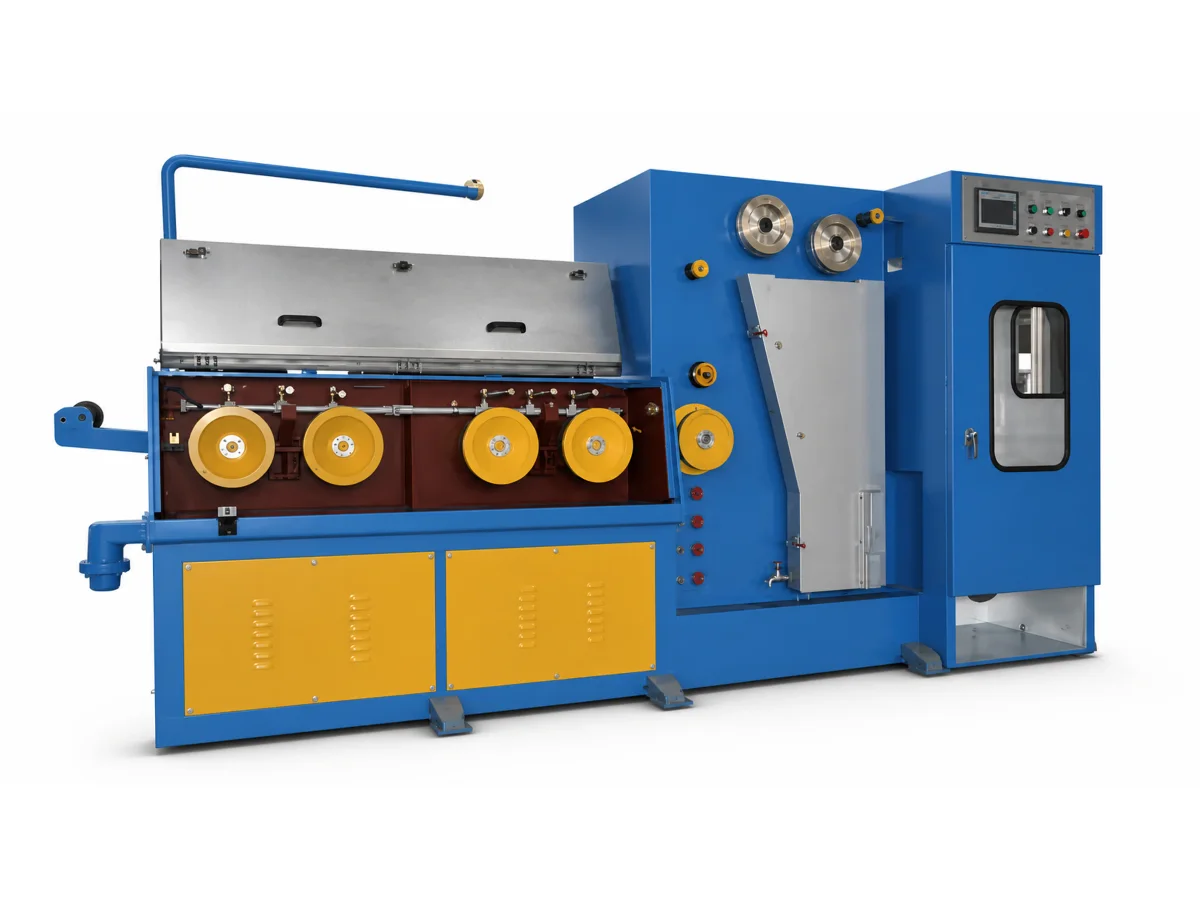
Wire drawing machine, existing 3D equipment reference3D equipment reference; final size and configuration to confirm
01 / Equipment configuration

تحضير الأسلاك

Prepare copper wire to the required diameter and material condition, only where this upstream stage is needed.

Route status
Upstream / if required
Source boundary
Wire drawing equipment; category checked against HONGKAI catalogue p. 45; 3D reference
Configuration
Copper grade, incoming size, wire diameter, condition, reel and inspection requirements
Key input
Specified incoming copper rod / wire

Copper grade, incoming size, wire diameter, condition, reel and inspection requirements

05 Manufacturing and integration

Keep Every Equipment Source and Responsibility Explicit

A coordinated production-line project does not mean one factory manufactures every machine. Each source and interface is defined in the approved proposal.

Control Cable, one coordinated project interface

Equipment source, contracting entity, integration boundary and service responsibility stay item-specific.

Proposal-defined scope
01 / HONGKAI manufacturing scope

مصنوع بواسطة HONGKAI

Core-insulation and outer-sheathing equipment only where expressly identified as HONGKAI-manufactured in the confirmed proposal.

  • Insulation and sheathing equipment identified in the proposal
  • Mechanical assembly and electrical-control scope only as defined for each identified item
  • Factory inspection or testing only where stated in the approved proposal
Final configuration and responsibility, To be confirmed
02 / Specialist manufacturing scope

متكاملة من مصنّعين متخصصين

Conductor formation, core laying-up and any specified foil or braid screening system. Sources and interfaces are defined for each item.

  • Conductor formation matched to the specified copper class
  • Core laying-up with controlled tension and identity management
  • Screen application only where required by the approved design
  • Source and contractual boundary stated in the proposal
مصدر المعدات ونطاقها، يُنتظر التأكيد
03 / Supporting systems

Supporting Equipment and Project Interfaces

Cooling, inspection, core identification, any required screen checks, take-up, packing and agreed utilities.

  • Exact functions and equipment source remain project-specific
  • Customer-side utilities and interface responsibilities
  • Installation, commissioning and training scope if agreed
Any HONGKAI-configured or supplied supporting items: To be confirmed in the proposal
06 مدخلات تخطيط المصنع

Plan the Factory Around the Confirmed Line Scope

حدد فقط المعلومات التي لديك بالفعل. تسجّل هذه القائمة الاستعداد للمراجعة ولا تحفظ أو تُرسل بيانات المشروع.

07 Quality checkpoints

Keep Core Identity Traceable Through Final Testing

Agree the inspection plan before equipment selection. Equipment illustrations show the named device only; finished-cable acceptance requires the agreed test methods and records.

Seven-core copper control cable with separate insulation, fillers and an outer sheath; unshielded construction illustrationConductor acceptance
Conductor acceptance

Check Conductors and Core Identity

Verify conductor construction and resistance, then maintain the approved colour or numbering scheme and core sequence through each process.

Wire count inside one conductor is not the number of insulated cores. The 3D cable is a structure illustration, not a test sample.
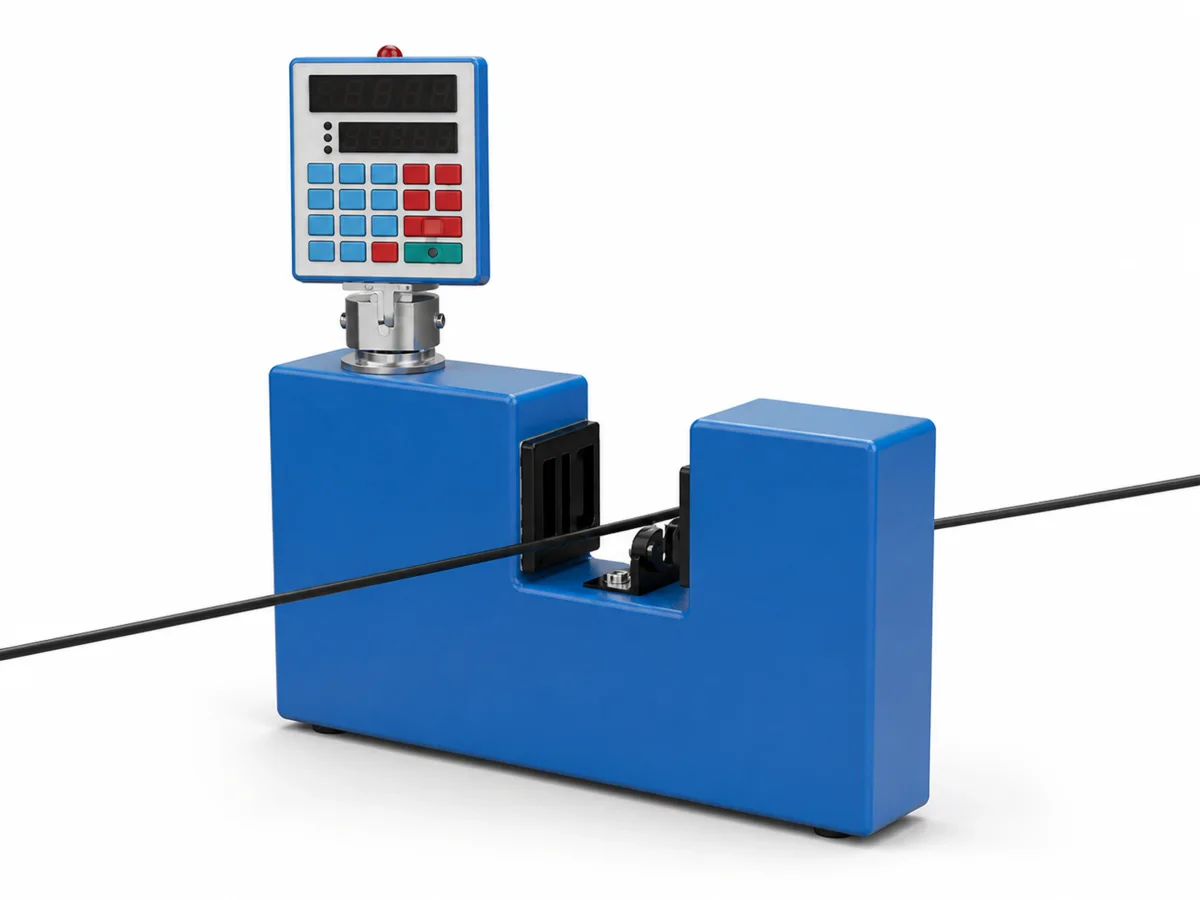
Laser outside-diameter gauge, existing 3D equipment referenceDimensional control
Dimensional control

Measure Diameter; Verify the Wall

Measure insulated-core and finished-cable diameters. Verify core insulation and outer-sheath wall thickness separately by the approved measurement method.

A laser outside-diameter gauge alone cannot establish minimum wall thickness. The acceptance method and tolerances must be defined.
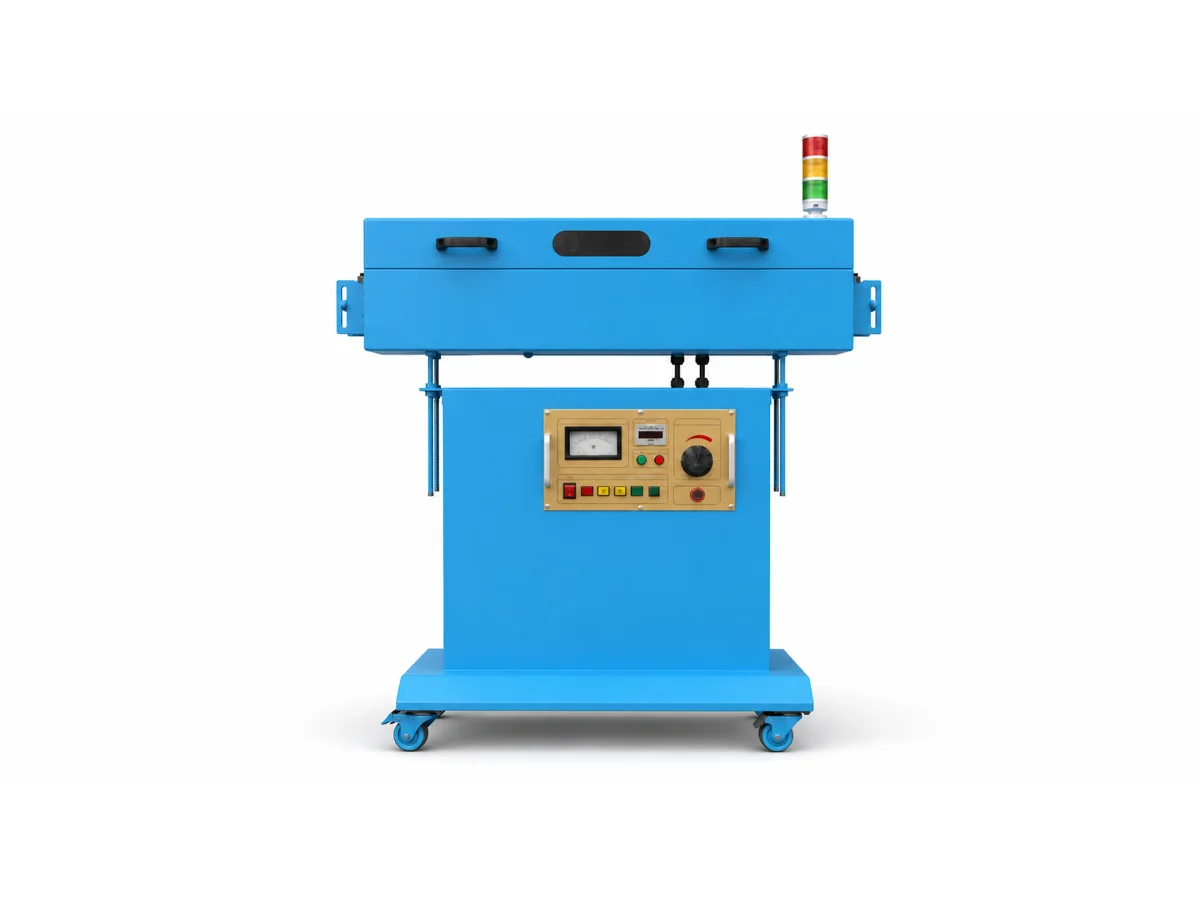
Insulated-core spark tester, existing 3D equipment referenceIn-line electrical check
In-line electrical check

Inspect the Dry Insulation

Cool and dry each insulated core before its specified spark test. Record faults and keep accepted core reels identifiable before cabling.

Core spark testing does not replace finished-cable electrical tests. Any sheath integrity test needs its own approved method and suitable electrical arrangement.
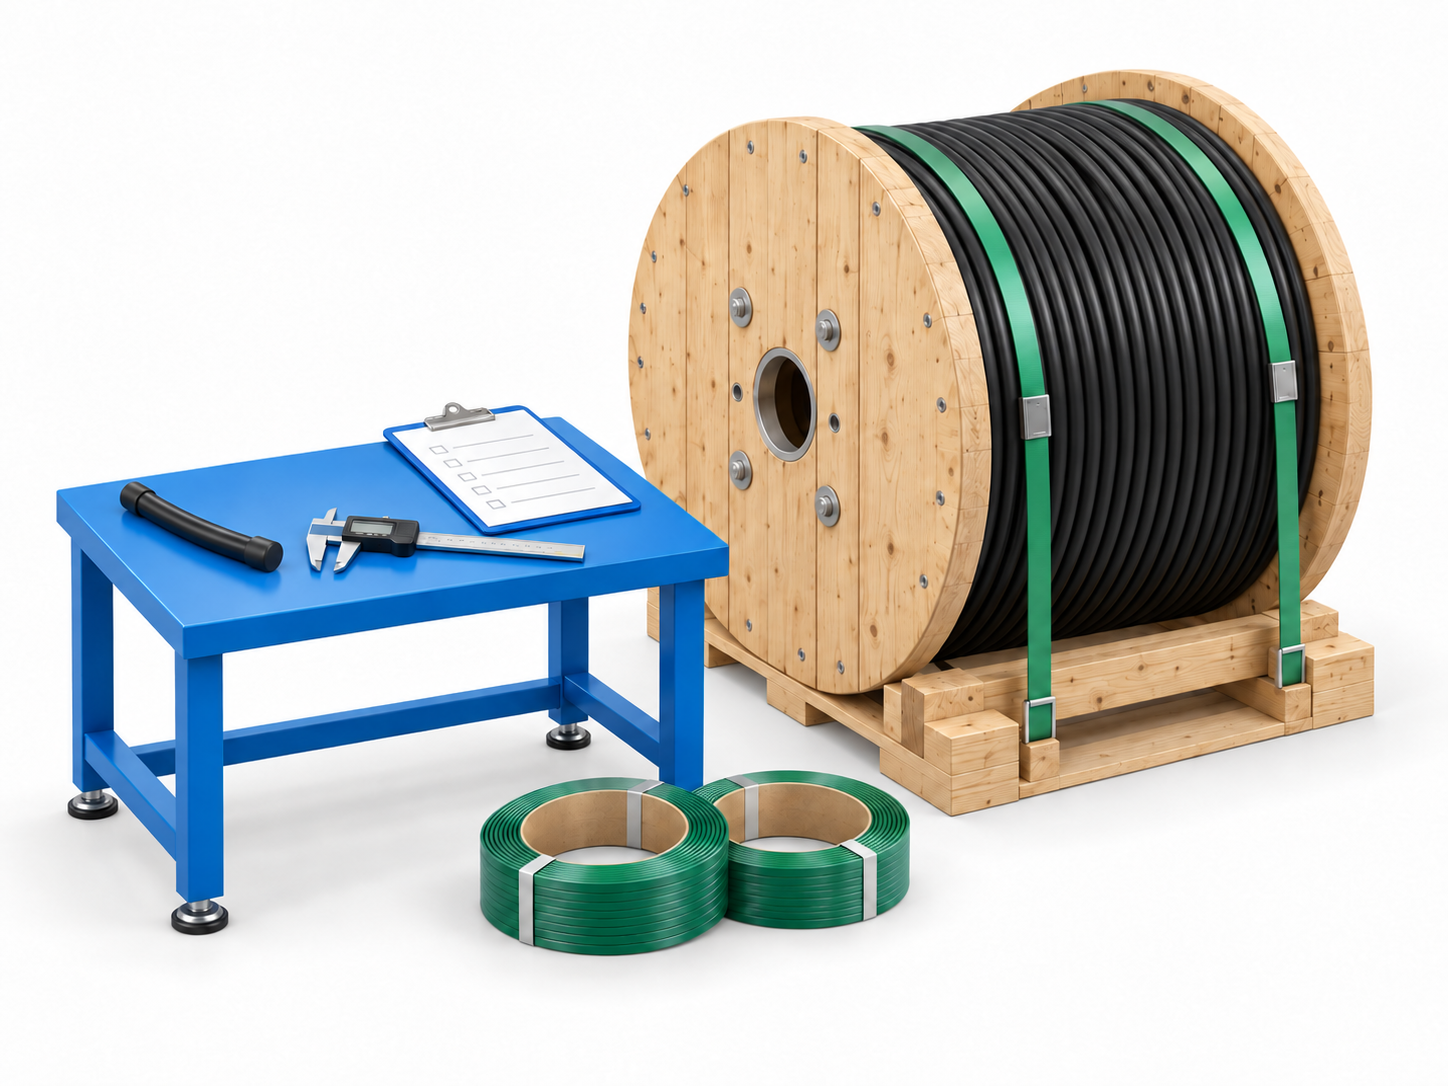
3D workflow illustration of a finished cable drum, dimensional inspection tools and packing recordsFinished-product release
Finished-product release

Verify Continuity and Packing

Confirm core identification and continuity, specified electrical and dimensional tests, and screen checks only where required. Verify cable marking, length and the agreed packing format.

Release the finished cable only against the agreed test results, identification, length and packing records.
Keep illustration and evidence separate. Add actual trial records, sample measurements and project acceptance documents once available. No performance or certification is inferred from a render.
Project records required
08 التعليمات

وضح المسار قبل طلب عرض سعر

These answers explain the decision path. They do not replace an approved cable design, technical solution, quotation or project proposal.

What does a control cable production line include?

The preliminary route includes copper-wire preparation and conductor formation where required, core insulation and identification, core checks, laying-up, outer sheathing, cooling and final tests. A screen application stage is added only for a specified screened construction.

Is every control cable screened?

No. The seven-core reference is unshielded. Foil, braid or combined screens belong to a separate approved construction. Select the required screen in the route review and provide its dimensions, material and acceptance requirements.

How are cores identified during production?

Use the colours or numbers specified by the approved cable design. Confirm the marking method, legibility and sequence before laying-up, then verify identification and continuity on the finished cable. The illustration does not establish a universal colour scheme.

Are conductor bunching and core laying-up the same operation?

No. Bunching or stranding forms one bare conductor from individual wires before insulation. Laying-up assembles separately insulated and identified cores. Choose both systems for the actual conductor class, core size, lay and reel format.

Can the same screening equipment apply foil and braid?

Do not assume interchangeability. Foil application needs suitable tape handling and overlap control; braiding uses a different application arrangement and coverage controls. Drain wires, separators and combined screens also require a defined process.

Does a flexible conductor automatically make the cable suitable for continuous movement?

No. Moving duty depends on the complete cable construction, materials, lay, bend conditions and qualification requirements. State fixed installation or the required movement duty before equipment and material selection.

Which checks are required on the finished control cable?

Agree core identification and continuity checks, conductor resistance, specified electrical and insulation tests, dimensions and marking. Add screen continuity or other screen-related acceptance only where the design requires it, then verify length and packing.

What information is needed to select the equipment?

Provide conductor area and class, wire construction, core count and identity, insulation and sheath compounds and walls, any screen specification, output mix, finished diameter and packing format. Models, speeds and supply responsibilities are confirmed in the proposal.

09 Control Cable project enquiry

Plan Your Control Cable Production Line

Share conductor class and size, core count and identification, insulation and sheath. If screening is required, include the foil or braid construction, drain wire and acceptance requirements.

Route currently on this page

  • عائلة الكابلاتكابل تحكم
  • Current route reviewPrepare copper wires / form conductors → Insulate and identify cores → Core checks → Lay up identified cores → Outer sheath → Cool, test and pack
  • Conductor inputsCopper class and size, core identity, optional screen design and sheath
  • Finished core countSeven cores in the artwork; actual count and identification to confirm.

Optional. Review the copied context before sending.

An enquiry requests a project-scope review. It does not confirm equipment configuration, material compatibility, price, delivery schedule, output, factory acceptance or project result.

قارن جميع حلول الكابلات

Control Cable Project Enquiry

Fields marked * are required. Technical inputs may remain to be confirmed.

The dedicated enquiry form has not been connected yet. Please contact HONGKAI through the project enquiry page.

Your contact details

من يجب أن يتلقى المتابعة الفنية؟
Include country code, if provided.

Conductor and cable construction

Define each conductor separately from cable core count; include core identification and any required screen.
Applicable product standard and rated voltage from the approved design.
Copper conductor class, wire construction and finished dimensions.
Area in mm², not the sum of all cores.
For stranded conductors, wire dimensions by layer if needed.
For stranded conductors; state solid where applicable.
Outside diameter before insulation, in mm.
Number of separately insulated cores in the finished cable.
Colour or number scheme, marking method, sequence and protective core as specified.
Approved insulation compound, grade and nominal / minimum wall.
Target and tolerance in mm.
Lay length, direction and bundle OD before sheathing, if known.
Only where specified by the cable drawing.
Specified sheath compound and nominal / minimum wall.
Target and tolerance after sheathing, in mm.
None, foil, braid or combined; material, coverage / overlap, drain wire and separators if required.
Flange and barrel diameter, width, bore, cable length and maximum loaded mass.
State the installation or movement conditions and required cable / screen tests.

Project requirements

Final range, output and equipment interfaces require technical review.
Cable size, quantity, unit, working hours and product mix.
اسحب وأفلت الملفات، , اختر الملفات لرفعها يمكنك تحميل ما يصل إلى 3 من الملفات.
Optional: PDF, JPG, JPEG or PNG. Up to 3 files, 10 MB each.
Use Add Viewed Route to Form, then review or edit the copied context.

اطلب الاقتباس

سوف نقوم بالرد عليك خلال 24 ساعة!!!