


Preparing for network cable UL Listing starts with the exact cable, intended installation type, manufacturing site and certification scope, before testing becomes the main task. The practical decision is not which machine can “make a UL cable,” but which controlled product and production system will be submitted and maintained.
UL Listing is a product-and-factory control program, not a one-time machine setting or a logo added after production. A factory should freeze the construction, confirm the applicable UL category with UL Solutions, prepare representative samples and evidence, and build ongoing material, process, marking and change controls before formal evaluation.
그만큼 HONGKAI LAN 케이블 생산 라인 connects conductor preparation, insulation, pair twisting, cabling, optional shielding, sheathing, testing and packing. UL Solutions remains responsible for determining the applicable certification program, investigation requirements, authorized markings and follow-up obligations. HONGKAI equipment configuration and factory trials should therefore support the approved cable specification; they cannot replace the certification body’s decision.
정확한 인증 객체로 시작하세요
The first document should name what will be certified or verified. “Cat6 with UL” is incomplete because safety Listing, transmission-performance Verification, cable assemblies and installed cabling are different objects with different evidence.
UL Solutions states that communications cable types such as CMP, CMR and CM may be certified to UL 444, while performance verification can be provided separately when required.1 이 회사의 전선 및 케이블 적용 가이드는 Listed, Classified, Certified 및 Verified 제품을 구분하며 사용자에게 해당 제품 카테고리와 표시를 확인하도록 안내한다.2
| Requested object | 반드시 확정되어야 하는 결정 | Primary evidence after approval | What the evidence does not automatically cover |
|---|---|---|---|
| Listed communications cable | Intended cable type, construction, ratings, manufacturing site and applicable category | Authorized Listing information, markings and current Product iQ record | Every other jacket, conductor, factory or cable family |
| Performance-verified LAN cable | Exact transmission-performance specification and product construction | Verification Mark and product-specific directory or certificate scope | Fire or installation-use Listing unless separately included |
| Communications cable assembly | Finished assembly construction, components and required evaluation | Assembly-specific Listing or Verification evidence | Bulk horizontal cable or installed channel performance |
| 설치된 영구 링크 또는 채널 | Site design, components, workmanship and field-test limit | Project field-test report | Factory certification of the cable itself |
Decision criterion: Ask the certifier to write the product category, target market, standard or program, cable type, manufacturing location, sample family and permitted marking. Keep safety Listing and performance Verification on separate lines even when the final product will carry both.
Common mistakes: A buyer asks for a “UL machine,” treats a Cat6 field-test PASS as a cable Listing, or assumes that a UL logo printed on the jacket proves current coverage. None of these defines the actual certification object.
Freeze the Saleable Cable Before Selecting Tests
The factory should submit a controlled saleable construction, not a broad marketing family. The conductor, insulation system, pair design, separator or shielding, jacket compound, cable type, manufacturing site and markings all need an identified revision.
UL Solutions’ current wire-and-cable overview names CMP, CMR and CM as different communications-cable types evaluated for their intended uses.1 The target cable type affects construction and evaluation; a factory should not select a jacket only by colour, processing convenience or a supplier’s generic “UL material” description.
In HONGKAI’s equipment-scoping discussions, five questions turn “I want to make UL network cable” into a usable starting brief:
| First question | What the buyer should provide | 장비 또는 증거 결정 |
|---|---|---|
| Is the saleable product bulk cable or a finished patch cord? | Box/reel length, conductor construction, flexibility, and whether connector assembly is included | Cable manufacture alone versus additional termination and assembly testing |
| Which constructions and categories are required now? | A drawing for each UTP, FTP, STP or SFTP request, with the exact pair/overall shield arrangement and present category range | Pair twisting, separator handling, foil wrapping, braiding and cabling route |
| What does “UL” mean in this purchase? | Target market, installation-use cable type, requested safety Listing and any separate performance Verification | Certification category and applicable test program to confirm with the certifier |
| What materials and geometry define the sample? | 도체, 절연체 및 재킷 식별; 솔리드 또는 발포 절연체; 치수 및 제어된 도면/BOM 개정 | 압출, 드로잉 인터페이스, 공구, 공정 제어 및 재료 시험 |
| 초기 라인은 무엇을 제공해야 하며, 무엇이 단지 향후 목표에 불과한가? | 제품 출시, 후속 모델, 요구 출력, 제조 현장 및 이용 가능한 실험실 역량 | 초기 장비 범위, 별도 가격 책정된 옵션, 전문 시험 인터페이스 및 FAT 승인 계획 |
Bulk packaging length is not a certification category. A customer’s shorthand such as a “300 m box” or a connection “within 100 m” must be replaced by the actual ordered length and test object. A patch cord is not simply every cable shorter than 100 m: Fluke Networks distinguishes the complete channel, including cords, from the fixed permanent link.3
Likewise, commercial shield abbreviations are not enough for machine selection. The approved cross-section must show whether shielding is around each pair, around the cabled core, or both, and identify foil, braid and drain-wire details. Keep each approved variant and its proposed print legend, reel/box label, packaging, manufacturing site and subcontracted stages in the product-definition record.
기계 경로는 이 정의를 따릅니다. The HONGKAI Cat5/Cat5e 참조 경로 shows insulation, pair twisting, cabling, sheathing, testing and packing as a connected process, with final construction and acceptance tied to the approved specification. A Cat6 or shielded construction may change separator handling, shielding equipment, process controls and laboratory scope; no common machine list proves that all variants belong in one certification family.
What to ask: Request written confirmation from UL Solutions about the applicable category and the documents, samples and manufacturing-site information required for the proposed construction. Do this before purchasing certification labels or promising a launch date.
결빙된 구조에 맞춘 쌍선 꼬임 및 절연
Pair geometry and insulation stability deserve attention before the final cable is tested. Changing the twisting route, conductor, insulation compound or foaming process after sample confirmation can change the product being submitted, even if the finished jacket still looks the same.
For pair twisting, compare the actual machine design, tension path, back-twist capability where required, payoff/take-up handling and demonstrated lay control. HONGKAI’s project experience includes triple-twist and other pair-twisting routes. For demanding constructions, Peter’s equipment-selection preference is to evaluate a suitable horizontal arrangement, but orientation alone is not proof of higher performance. Require trials on the intended conductor and insulation, agreed pitch measurements and downstream cable results before accepting a configuration.
Conductor consistency and insulation geometry are separate acceptance items. The conductor’s material, dimensions, surface condition and electrical checks should follow the product specification. For the insulating layer around each conductor, specify the compound and whether the design uses solid insulation, chemical foaming or physical foaming. Do not confuse core-wire insulation with the finished outer jacket, or assume that a familiar PVC grade is suitable for every LAN construction or cable fire rating.
Foaming is a process choice, not an automatic category upgrade or UL approval. Maillefer’s telecom-insulation documentation independently illustrates that solid and chemical-foam constructions require defined materials and line configurations, with drawing, extrusion and measurement functions coordinated as a system.4 Those examples are technical context, not HONGKAI model specifications. A HONGKAI proposal must separately confirm its compound compatibility, extrusion/foaming arrangement, tooling, concentricity control and agreed measurement provision. Moving between solid, chemical-foam and physical-foam designs requires a new compatibility and evidence review; it should not be treated as a recipe-only substitution.
Evidence to request: Freeze the conductor and compound identities, pair lay plan, insulation dimensions, concentricity definition and, for a foamed construction, the foaming-degree definition and test method. Define acceptance limits from the approved product and trial plan; do not copy a generic machine brochure value into the certification specification.
One project described by HONGKAI illustrates why the product range must precede the machine list: it covers UTP and SFTP constructions through Cat6A, with Cat7 as a later target. The discussed route combines drawing with chemical-foam insulation, triple twisting, active foil wrapping at cabling and a separately configured sheathing route. Different constructions may require different tape-handling provisions. This is a configuration example, not evidence that every variant was produced, that Cat7 was achieved, or that any product obtained UL Listing. Shielding and any protective metal-tape layer must be shown separately on the approved drawing.
통제된 순서로 평가 패키지를 구성하세요
The certification project should move from scope to construction evidence, representative samples, formal evaluation and production authorization. Individual projects vary, and UL Solutions describes the typical lifecycle as quote, testing and follow-up rather than a universal fixed timetable.5
| Sequence | Controlled output | 다음 단계 전의 질문 |
|---|---|---|
| 01 — Scope | 케이블 유형, 대상 시장, 제조 현장, 안전 인증 및 별도의 성능 검증 | 인증 기관이 의도된 프로그램을 확인했습니까? |
| 02 — Construction | 도면, BOM, 공정 경로, 마킹 제안, 공급업체 및 변경 절차 | 시험 사양서에 구조 개정 번호가 명시되어 있습니까? |
| 03 — Evidence | 재료, 치수, 전기적 특성 및 공정 기록이 포함된 대표 샘플 | 제출된 각 샘플을 실제 제작물과 연결할 수 있습니까? |
| 04 — Continuing control | 공식 평가 결과, 초기 검사 준비 및 승인된 마킹/후속 통제 | 공장은 승인된 범위를 유지할 준비가 되어 있습니까? |
Evidence to request: Keep the certifier’s proposal, product-category decision, sample instructions, construction description, test plan, findings, approved revisions, follow-up procedure, marking authorization and factory-inspection records under one controlled project number.
참고: 내부 또는 외부 실험실 검사를 통과한 사전 인증 샘플은 유용한 엔지니어링 증거입니다. 그러나 이는 UL 마크를 적용할 수 있는 승인을 의미하지 않습니다.
모든 생산 단계를 지속적인 규정 준수에 연결하세요
A factory needs a control plan that can reproduce the evaluated construction. The useful question for each stage is: what product characteristic is created here, what record proves control, and what change requires technical review?
The production route can be designed backward from the approved cable. The table below is a proposed control map for the factory and certifier to review; it is not a substitute for the UL Follow-Up Services procedure.
| 생산 단계 | 제어된 입력 또는 설정 | Retained evidence | 검토를 유도해야 하는 변경 사항 |
|---|---|---|---|
| 도체 준비 | 재질, 구조, 출처 및 완성 도체 상태 | 관리 계획에 따라 요구되는 입고 시의 신원, 로트, 치수 및 저항 기록 | 재질, 소스, 도금 또는 도체 구조 |
| 심선 절연체 | Approved compound, tooling, diameter, concentricity, colour and foaming system if used | Compound lot, line setup, dimensional data, foaming-degree results when applicable, and nonconformance record | 컴파운드 등급 또는 공급업체, 솔리드/폼 구조, 발포 방식 또는 툴링 |
| 페어 비틀기 | Pair identity, lay plan, tension route and reel traceability | 설정 시트, 측정된 피치, 쌍/릴 ID 및 합의된 공정 중 검사 | Lay plan, machine route or tension-control method |
| 케이블링 및 차폐 | Pair position, separator, foil, drain wire or braid construction | 해당되는 경우, 트래블러, 재료 로트, 코어 형상 및 연속성 기록 | Separator, shield material, overlap, drain wire or braid design |
| 피복 및 마킹 | Approved jacket compound, wall, finished size, print legend and surface condition | Jacket lot, dimensional record, print approval and reel identity | 재킷 등급 또는 공급업체, 케이블 유형, 정격 또는 인쇄 표시 |
| Final test and packing | 정의된 샘플, 방법, 수용 기준 및 포장 라벨 | Raw results, disposition, reel/box traceability and label control | 시험 방법, 샘플 기준, 소프트웨어 한계, 포장 또는 라벨 내용 |
The earlier Cat6 공장 규정 준수 가이드 explains why a final analyzer cannot repair uncontrolled conductor, insulation or pair geometry. The same logic matters here: certification evidence must be linked to the process that made the sample and to the production records that will continue after approval.
How to verify: Select one finished reel or box and trace it backward to the approved construction, material lots, process records, inspection results, final test and authorized label. Then select one material or process change and show who decides whether certification review is required before production resumes.
UL 결정과 공장 사전 검사를 분리
Factory and third-party prechecks reduce avoidable risk, but UL Solutions controls the formal investigation scope, sample requirements, acceptance decision and authorization to use its Mark. The factory laboratory should support the submission without describing itself as the certifier.
Before formal evaluation, the factory can check whether the proposed construction is stable enough to submit. Useful preparation may include dimensional checks, conductor and insulation records, electrical prechecks, fire-test preparation by an appropriate laboratory, marking review and repeat builds from more than one production run. The exact method, equipment, sample count and pass/fail source must come from the agreed certification plan and applicable requirements.
For the equipment FAT, HONGKAI’s practical record priorities are measured pair lay/pitch, insulation concentricity and foaming degree whenever foamed insulation is used. Do not replace the last item with an operator’s observation that the insulation “looks foamed.” Agree the measurement definition, method, instrument and sampling locations before the trial, then retain actual results, units, acceptance source, instrument identity, operator/date and disposition.
Link these records to the drawing revision, machine setup, conductor and compound lots, trial reel and retained sample IDs. Record the trial conditions actually demonstrated; one successful sample is not evidence of an untested speed, material or product range. These FAT measurements support sample preparation and repeatability, but they are not a complete UL test program.

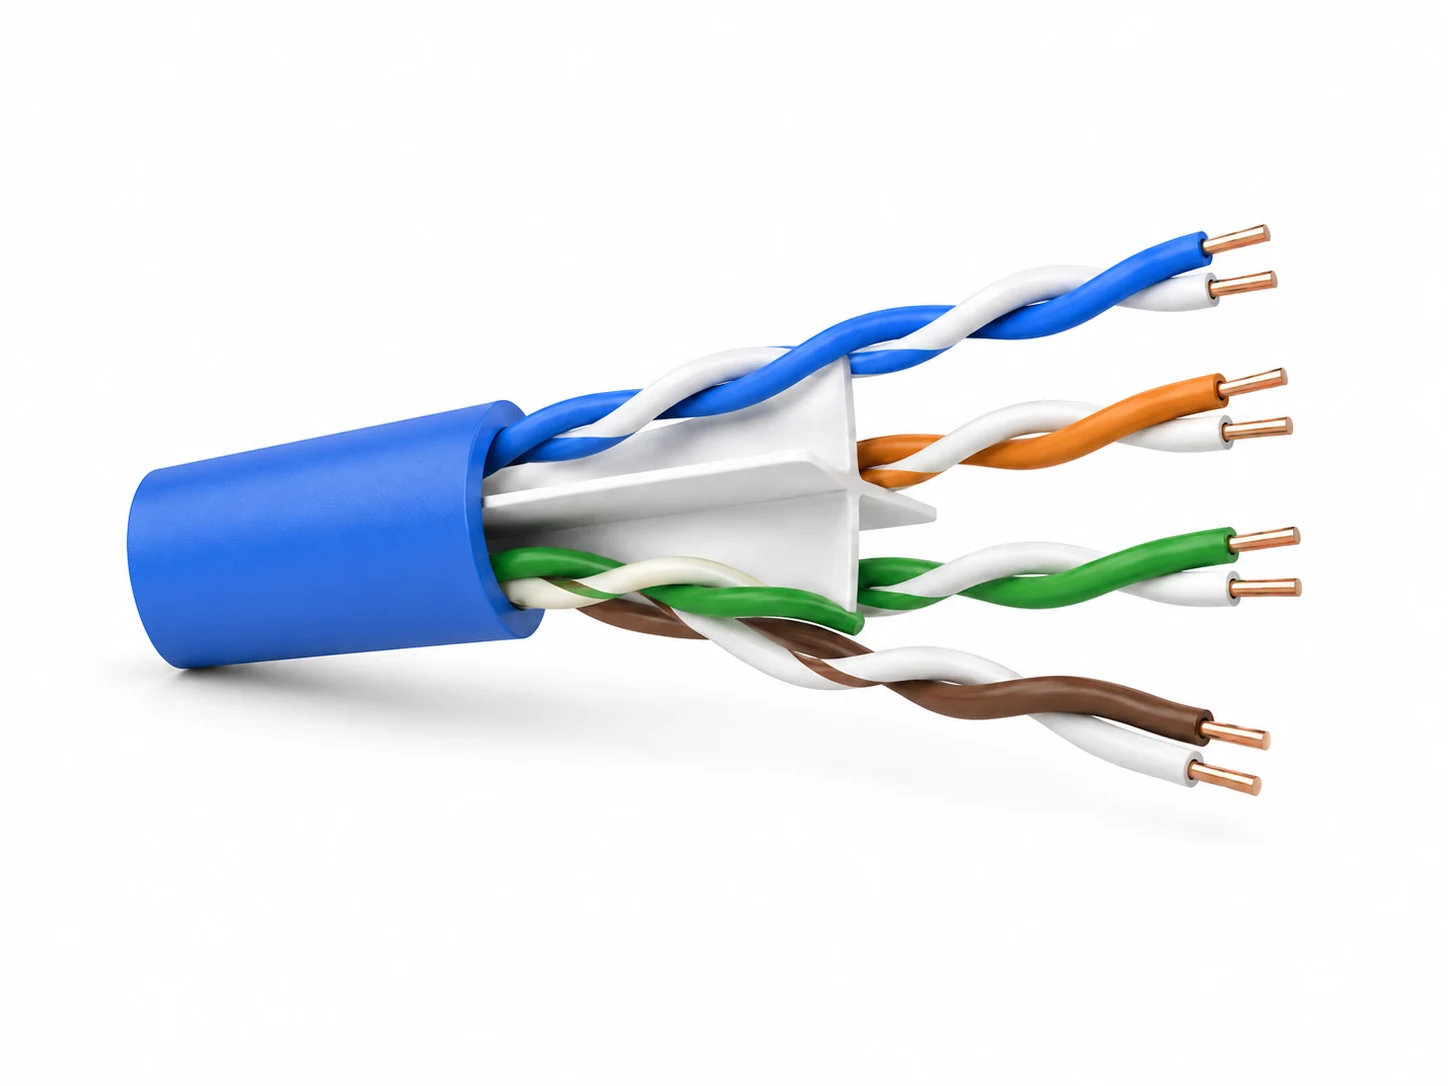
Explanatory 3D illustration, not a real test report or certification result. Retain measured pitch, concentricity and foaming degree when applicable, linked to the actual sample.
| Evidence layer | Responsible party | 지원하는 결정 |
|---|---|---|
| 기계 설정 및 공정 중 기록 | 장비 공급업체의 의견을 반영한 케이블 공장 | 평가된 구조가 정의된 조건 하에서 재현될 수 있는지 여부 |
| 내부 실험실 사전 점검 | 케이블 공장 또는 자격을 갖춘 실험실 | 샘플이 공식 제출 준비가 되었는지 여부 및 공정이 불안정한 위치 |
| 공식 평가 및 인증 결정 | 합의된 프로그램에 따른 UL 솔루션 | Whether the identified product and site qualify for the authorized certification scope |
| Independent transmission-performance Verification | 요청 시 UL Solutions 또는 다른 지정된 프로그램 | Whether the identified cable meets the named performance specification within that program’s scope |
| 설치된 케이블링 현장 테스트 | Installer, project test team or qualified field service | 설치된 링크 또는 채널이 프로젝트의 현장 기준을 충족하는지 여부 |
Red flags: The submission sample was made with unrecorded hand adjustments; the production BOM differs from the tested sample; a third-party report does not identify the exact construction; or the factory plans to replace compounds after approval without a documented review path.
마킹 및 후속 서비스를 위해 공장을 준비하세요
UL Listing continues after the initial evaluation. The factory must protect the approved construction, authorized labels, production records, inspection access and change-control process for as long as it produces marked cable.
UL Solutions states that the complete Listing Mark on the tag attached to the reel or smallest unit container is the proof that a particular wire or cable unit is UL Listed; surface printing is supplemental.2 The same guide says holographic labels are required for Listed communications cable and several related wire-and-cable categories. UL Solutions also explains that initial product inspection and follow-up services are part of the customer lifecycle.5
공장 준비 완료 파일은 다음을 명시해야 합니다:
- 라벨에 대한 접근을 통제하고 사용 내역을 조정하는 사람은 누구인가;
- 승인된 구조물과 마킹 도안이 저장되는 곳;
- how incoming materials are checked against approved identities;
- 릴 또는 박스와 생산 및 검사 기록이 어떻게 연결되는지;
- 비적합 재료 및 표시된 제품이 어떻게 격리되는지;
- how factory inspectors receive current records and production access;
- how product, material, supplier, process, site or marking changes are reviewed;
- 구식 도면, 라벨 및 작업 지침서가 사용에서 어떻게 제거되는지.
In HONGKAI’s preparation discussions, the easily missed items are raw-material traceability, retrievable production/test data and usable work instructions. Test that system before preparing the submission: ask an operator to retrieve the instruction revision used for one sample, identify its material lots and locate the corresponding raw results. A folder of disconnected screenshots does not establish that chain.
Common mistakes: The jacket print is treated as the only Listing evidence; labels can be taken without reconciliation; approved and unapproved compounds share the same internal name; or production changes are implemented before the certification owner reviews their effect.
근거를 중심으로 RFQ 및 책임 매트릭스 작성
The cable factory, machinery supplier, material suppliers, laboratories and UL Solutions have different responsibilities. A complete project defines the handoffs instead of asking one party to promise “UL approval.”
| Deliverable | 케이블 공장 | HONGKAI equipment scope | UL Solutions 또는 전문 기관 |
|---|---|---|---|
| Target cable and certification scope | Own the saleable product decision and application | 승인된 케이블 경로를 장비 및 인터페이스 관련 질문으로 번역하세요. | Confirm applicable certification category and evaluation program |
| Controlled construction and BOM | 자체 도면, 자재, 공급업체 및 개정판 | Confirm machine compatibility with the signed process inputs | Review construction within the formal project scope |
| Trial production and records | Provide materials, operators and product traceability | 합의된 기계 설정, FAT 및 공정 기록 산출물을 지원합니다. | 계약에 명시된 경우에만 공식적인 증거를 정의하거나 입회하십시오. |
| Laboratory evidence | Own sample identity and internal release records | Provide agreed measurement interfaces; specialist test equipment stays separately scoped | 자체 책임 하에 공식 평가 또는 전문가 테스트를 수행합니다. |
| Factory control and changes | Operate approved procedures, labels and change review | 기계 구성 및 승인된 변경 사항 문서화 | Conduct applicable inspection, follow-up and certification review |
HONGKAI can develop the overall manufacturing-equipment proposal, configure the relevant LAN stages and document agreed FAT outputs. Its own delivery responsibility is the equipment scope stated in the contract. Specialist laboratory and inspection equipment must be separately sourced and assigned; inclusion in an overall project proposal does not mean HONGKAI manufactures every instrument or acts as the certification body. Certification decisions, authorized UL markings and Follow-Up Services remain with UL Solutions under the applicable program, not with a machinery FAT.
Evidence to request: Add a certification-readiness appendix to the RFQ. It should list the target cable, product category to be confirmed, controlled materials, process route, trial samples, factory records, laboratory boundaries, label responsibility, factory-inspection preparation, change-review owner and all explicit exclusions.
Note: The strongest purchase specification does not promise that a machine will obtain UL Listing. It requires a reproducible cable route and evidence system that the factory can submit, audit and maintain under the certification body’s approved scope.
-
UL Solutions 와이어 및 케이블 개요, describing communications-cable certification for CMP, CMR and CM under UL 444 and separate performance-verification services. ↩ ↩
-
UL Solutions Wire and Cable Application Guide, explaining product categories, certification marks, Product iQ and wire-and-cable marking evidence. ↩ ↩
-
채널 테스트 및 영구 링크에 관한 플루크 네트웍스, distinguishing the complete channel from fixed cabling and its patch cords. ↩
-
Maillefer 통신 케이블 절연, illustrating solid/chemical-foam insulation and coordinated drawing, extrusion and measurement functions; not a specification for HONGKAI equipment. ↩
-
UL Solutions New Client Welcome and Resources, 일반적인 견적-시험-후속 조치 사이클, 초기 제품 검사 및 후속 서비스를 설명합니다. ↩ ↩