

Preparing for network cable UL Listing starts with the exact cable, intended installation type, manufacturing site and certification scope, before testing becomes the main task. The practical decision is not which machine can “make a UL cable,” but which controlled product and production system will be submitted and maintained.
UL Listing is a product-and-factory control program, not a one-time machine setting or a logo added after production. A factory should freeze the construction, confirm the applicable UL category with UL Solutions, prepare representative samples and evidence, and build ongoing material, process, marking and change controls before formal evaluation.
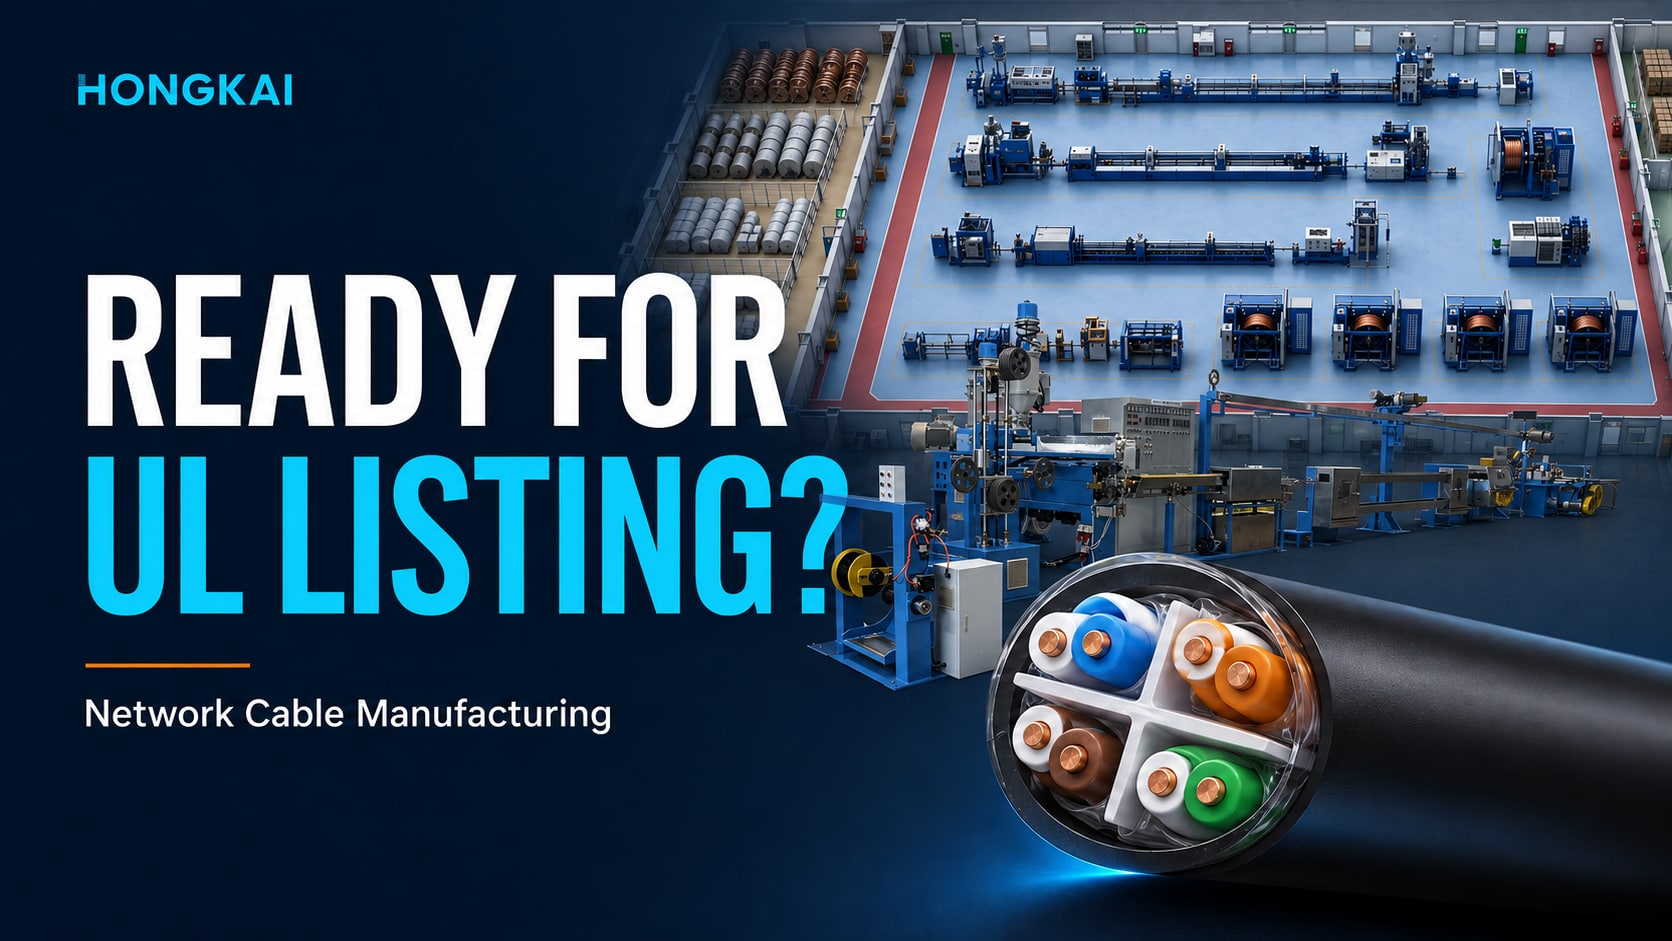
The HONGKAI LAN cable production route connects conductor preparation, insulation, pair twisting, cabling, optional shielding, sheathing, testing and packing. UL Solutions remains responsible for determining the applicable certification program, investigation requirements, authorized markings and follow-up obligations. HONGKAI equipment configuration and factory trials should therefore support the approved cable specification; they cannot replace the certification body’s decision.
Начните с точного объекта сертификации
The first document should name what will be certified or verified. “Cat6 with UL” is incomplete because safety Listing, transmission-performance Verification, cable assemblies and installed cabling are different objects with different evidence.
UL Solutions states that communications cable types such as CMP, CMR and CM may be certified to UL 444, while performance verification can be provided separately when required.1 Его Руководство по применению проводов и кабелей также разделяет продукцию на категории Listed, Classified, Certified и Verified и рекомендует пользователям проверять соответствующую категорию продукции и маркировку.2
| Requested object | Решение, которое должно быть заморожено | Первичные доказательства после утверждения | Что доказательства не охватывают автоматически |
|---|---|---|---|
| Перечисленный кабель связи | Предполагаемый тип кабеля, конструкция, характеристики, место производства и применимая категория | Информация об авторизованном перечне, маркировка и текущая запись Product iQ | Every other jacket, conductor, factory or cable family |
| Performance-verified LAN cable | Exact transmission-performance specification and product construction | Verification Mark and product-specific directory or certificate scope | Fire or installation-use Listing unless separately included |
| Communications cable assembly | Finished assembly construction, components and required evaluation | Assembly-specific Listing or Verification evidence | Bulk horizontal cable or installed channel performance |
| Установленное постоянное соединение или канал | Site design, components, workmanship and field-test limit | Project field-test report | Factory certification of the cable itself |
Decision criterion: Ask the certifier to write the product category, target market, standard or program, cable type, manufacturing location, sample family and permitted marking. Keep safety Listing and performance Verification on separate lines even when the final product will carry both.
Common mistakes: A buyer asks for a “UL machine,” treats a Cat6 field-test PASS as a cable Listing, or assumes that a UL logo printed on the jacket proves current coverage. None of these defines the actual certification object.
Freeze the Saleable Cable Before Selecting Tests
The factory should submit a controlled saleable construction, not a broad marketing family. The conductor, insulation system, pair design, separator or shielding, jacket compound, cable type, manufacturing site and markings all need an identified revision.
UL Solutions’ current wire-and-cable overview names CMP, CMR and CM as different communications-cable types evaluated for their intended uses.1 The target cable type affects construction and evaluation; a factory should not select a jacket only by colour, processing convenience or a supplier’s generic “UL material” description.
In HONGKAI’s equipment-scoping discussions, five questions turn “I want to make UL network cable” into a usable starting brief:
| First question | What the buyer should provide | Equipment or evidence decision |
|---|---|---|
| Is the saleable product bulk cable or a finished patch cord? | Box/reel length, conductor construction, flexibility, and whether connector assembly is included | Cable manufacture alone versus additional termination and assembly testing |
| Which constructions and categories are required now? | A drawing for each UTP, FTP, STP or SFTP request, with the exact pair/overall shield arrangement and present category range | Pair twisting, separator handling, foil wrapping, braiding and cabling route |
| What does “UL” mean in this purchase? | Целевой рынок, тип кабеля для монтажа и эксплуатации, запрашиваемый сертификат безопасности и любая отдельная проверка характеристик | Категория сертификации и применимая испытательная программа для подтверждения у органа по сертификации |
| Какие материалы и геометрия определяют образец? | Conductor, insulation and jacket identities; solid or foamed insulation; dimensions and controlled drawing/BOM revisions | Экструзия, интерфейсы волочения, оснастка, управление процессом и испытания материалов |
| What must the initial line deliver, and what is only a future target? | Запуск продукции, последующие варианты, требуемая мощность, производственная площадка и доступные лабораторные возможности | Исходная комплектация оборудования, опции с отдельной ценой, интерфейсы для специализированных испытаний и план приёмки на заводе-изготовителе (FAT) |
Bulk packaging length is not a certification category. A customer’s shorthand such as a “300 m box” or a connection “within 100 m” must be replaced by the actual ordered length and test object. A patch cord is not simply every cable shorter than 100 m: Fluke Networks distinguishes the complete channel, including cords, from the fixed permanent link.3
Likewise, commercial shield abbreviations are not enough for machine selection. The approved cross-section must show whether shielding is around each pair, around the cabled core, or both, and identify foil, braid and drain-wire details. Keep each approved variant and its proposed print legend, reel/box label, packaging, manufacturing site and subcontracted stages in the product-definition record.
Маршрут станка следует этому определению. The Эталонный маршрут HONGKAI Cat5/Cat5e shows insulation, pair twisting, cabling, sheathing, testing and packing as a connected process, with final construction and acceptance tied to the approved specification. A Cat6 or shielded construction may change separator handling, shielding equipment, process controls and laboratory scope; no common machine list proves that all variants belong in one certification family.
What to ask: Request written confirmation from UL Solutions about the applicable category and the documents, samples and manufacturing-site information required for the proposed construction. Do this before purchasing certification labels or promising a launch date.
Согласование парного скручивания и изоляции с замороженной конструкцией
Pair geometry and insulation stability deserve attention before the final cable is tested. Changing the twisting route, conductor, insulation compound or foaming process after sample confirmation can change the product being submitted, even if the finished jacket still looks the same.
For pair twisting, compare the actual machine design, tension path, back-twist capability where required, payoff/take-up handling and demonstrated lay control. HONGKAI’s project experience includes triple-twist and other pair-twisting routes. For demanding constructions, Peter’s equipment-selection preference is to evaluate a suitable horizontal arrangement, but orientation alone is not proof of higher performance. Require trials on the intended conductor and insulation, agreed pitch measurements and downstream cable results before accepting a configuration.
Conductor consistency and insulation geometry are separate acceptance items. The conductor’s material, dimensions, surface condition and electrical checks should follow the product specification. For the insulating layer around each conductor, specify the compound and whether the design uses solid insulation, chemical foaming or physical foaming. Do not confuse core-wire insulation with the finished outer jacket, or assume that a familiar PVC grade is suitable for every LAN construction or cable fire rating.
Foaming is a process choice, not an automatic category upgrade or UL approval. Maillefer’s telecom-insulation documentation independently illustrates that solid and chemical-foam constructions require defined materials and line configurations, with drawing, extrusion and measurement functions coordinated as a system.4 Those examples are technical context, not HONGKAI model specifications. A HONGKAI proposal must separately confirm its compound compatibility, extrusion/foaming arrangement, tooling, concentricity control and agreed measurement provision. Moving between solid, chemical-foam and physical-foam designs requires a new compatibility and evidence review; it should not be treated as a recipe-only substitution.
Evidence to request: Freeze the conductor and compound identities, pair lay plan, insulation dimensions, concentricity definition and, for a foamed construction, the foaming-degree definition and test method. Define acceptance limits from the approved product and trial plan; do not copy a generic machine brochure value into the certification specification.
One project described by HONGKAI illustrates why the product range must precede the machine list: it covers UTP and SFTP constructions through Cat6A, with Cat7 as a later target. The discussed route combines drawing with chemical-foam insulation, triple twisting, active foil wrapping at cabling and a separately configured sheathing route. Different constructions may require different tape-handling provisions. This is a configuration example, not evidence that every variant was produced, that Cat7 was achieved, or that any product obtained UL Listing. Shielding and any protective metal-tape layer must be shown separately on the approved drawing.
Соберите оценочный пакет в контролируемой последовательности
The certification project should move from scope to construction evidence, representative samples, formal evaluation and production authorization. Individual projects vary, and UL Solutions describes the typical lifecycle as quote, testing and follow-up rather than a universal fixed timetable.5
| Sequence | Controlled output | Вопрос перед следующим этапом |
|---|---|---|
| 01 — Scope | Тип кабеля, целевой рынок, производственная площадка, перечень требований безопасности и любая отдельная проверка характеристик | Подтвердил ли орган по сертификации предполагаемую программу? |
| 02 — Construction | Drawing, BOM, process route, marking proposal, suppliers and change procedure | Указывает ли пробная спецификация на ревизию конструкции? |
| 03 — Evidence | Репрезентативные образцы с записями о материале, размерах, электрических характеристиках и технологическом процессе | Можно ли проследить каждый представленный образец до фактической сборки? |
| 04 — Continuing control | Результаты формальной оценки, подготовка к первоначальной инспекции и авторизованная маркировка/контрольные мероприятия | Готов ли завод поддерживать утвержденный объем работ? |
Evidence to request: Keep the certifier’s proposal, product-category decision, sample instructions, construction description, test plan, findings, approved revisions, follow-up procedure, marking authorization and factory-inspection records under one controlled project number.
Примечание: образец, прошедший предварительную сертификацию и успешно проверенный во внутренней или внешней лаборатории, является полезным инженерным подтверждением. Однако это не дает разрешения на нанесение знака UL.
Свяжите каждый этап производства с непрерывным соблюдением требований
A factory needs a control plan that can reproduce the evaluated construction. The useful question for each stage is: what product characteristic is created here, what record proves control, and what change requires technical review?
The production route can be designed backward from the approved cable. The table below is a proposed control map for the factory and certifier to review; it is not a substitute for the UL Follow-Up Services procedure.
| Production stage | Controlled input or setting | Retained evidence | Change that should trigger review |
|---|---|---|---|
| Подготовка проводника | Material, construction, source and finished conductor condition | Incoming identity, lot, dimensional and resistance records required by the control plan | Material, source, plating or conductor construction |
| Изоляция токопроводящей жилы | Approved compound, tooling, diameter, concentricity, colour and foaming system if used | Compound lot, line setup, dimensional data, foaming-degree results when applicable, and nonconformance record | Compound grade or supplier, solid/foam construction, foaming route or tooling |
| Скручивание пар | Идентификация пары, схема скрутки, маршрут натяжения и прослеживаемость барабана | Setup sheet, measured pitch, pair/reel ID and agreed in-process checks | Lay plan, machine route or tension-control method |
| Кабели и экранирование | Pair position, separator, foil, drain wire or braid construction | Путевой лист, партии материалов, геометрия сердечника и записи о непрерывности, где применимо | Separator, shield material, overlap, drain wire or braid design |
| Оболочка и маркировка | Approved jacket compound, wall, finished size, print legend and surface condition | Партия оболочки, размерные записи, утверждение чертежа и идентификация барабана | Jacket grade or supplier, cable type, rating or print legend |
| Финальная проверка и упаковка | Defined sample, method, acceptance source and packaging label | Необработанные результаты, решение, прослеживаемость бухты/коробки и контроль маркировки | Метод испытания, основа отбора образцов, программное ограничение, упаковка или содержание маркировки |
The earlier Руководство по соответствию завода стандарту Cat6 explains why a final analyzer cannot repair uncontrolled conductor, insulation or pair geometry. The same logic matters here: certification evidence must be linked to the process that made the sample and to the production records that will continue after approval.
How to verify: Select one finished reel or box and trace it backward to the approved construction, material lots, process records, inspection results, final test and authorized label. Then select one material or process change and show who decides whether certification review is required before production resumes.
Отделите предварительные проверки на заводе от решения UL
Factory and third-party prechecks reduce avoidable risk, but UL Solutions controls the formal investigation scope, sample requirements, acceptance decision and authorization to use its Mark. The factory laboratory should support the submission without describing itself as the certifier.
Before formal evaluation, the factory can check whether the proposed construction is stable enough to submit. Useful preparation may include dimensional checks, conductor and insulation records, electrical prechecks, fire-test preparation by an appropriate laboratory, marking review and repeat builds from more than one production run. The exact method, equipment, sample count and pass/fail source must come from the agreed certification plan and applicable requirements.
For the equipment FAT, HONGKAI’s practical record priorities are measured pair lay/pitch, insulation concentricity and foaming degree whenever foamed insulation is used. Do not replace the last item with an operator’s observation that the insulation “looks foamed.” Agree the measurement definition, method, instrument and sampling locations before the trial, then retain actual results, units, acceptance source, instrument identity, operator/date and disposition.
Link these records to the drawing revision, machine setup, conductor and compound lots, trial reel and retained sample IDs. Record the trial conditions actually demonstrated; one successful sample is not evidence of an untested speed, material or product range. These FAT measurements support sample preparation and repeatability, but they are not a complete UL test program.

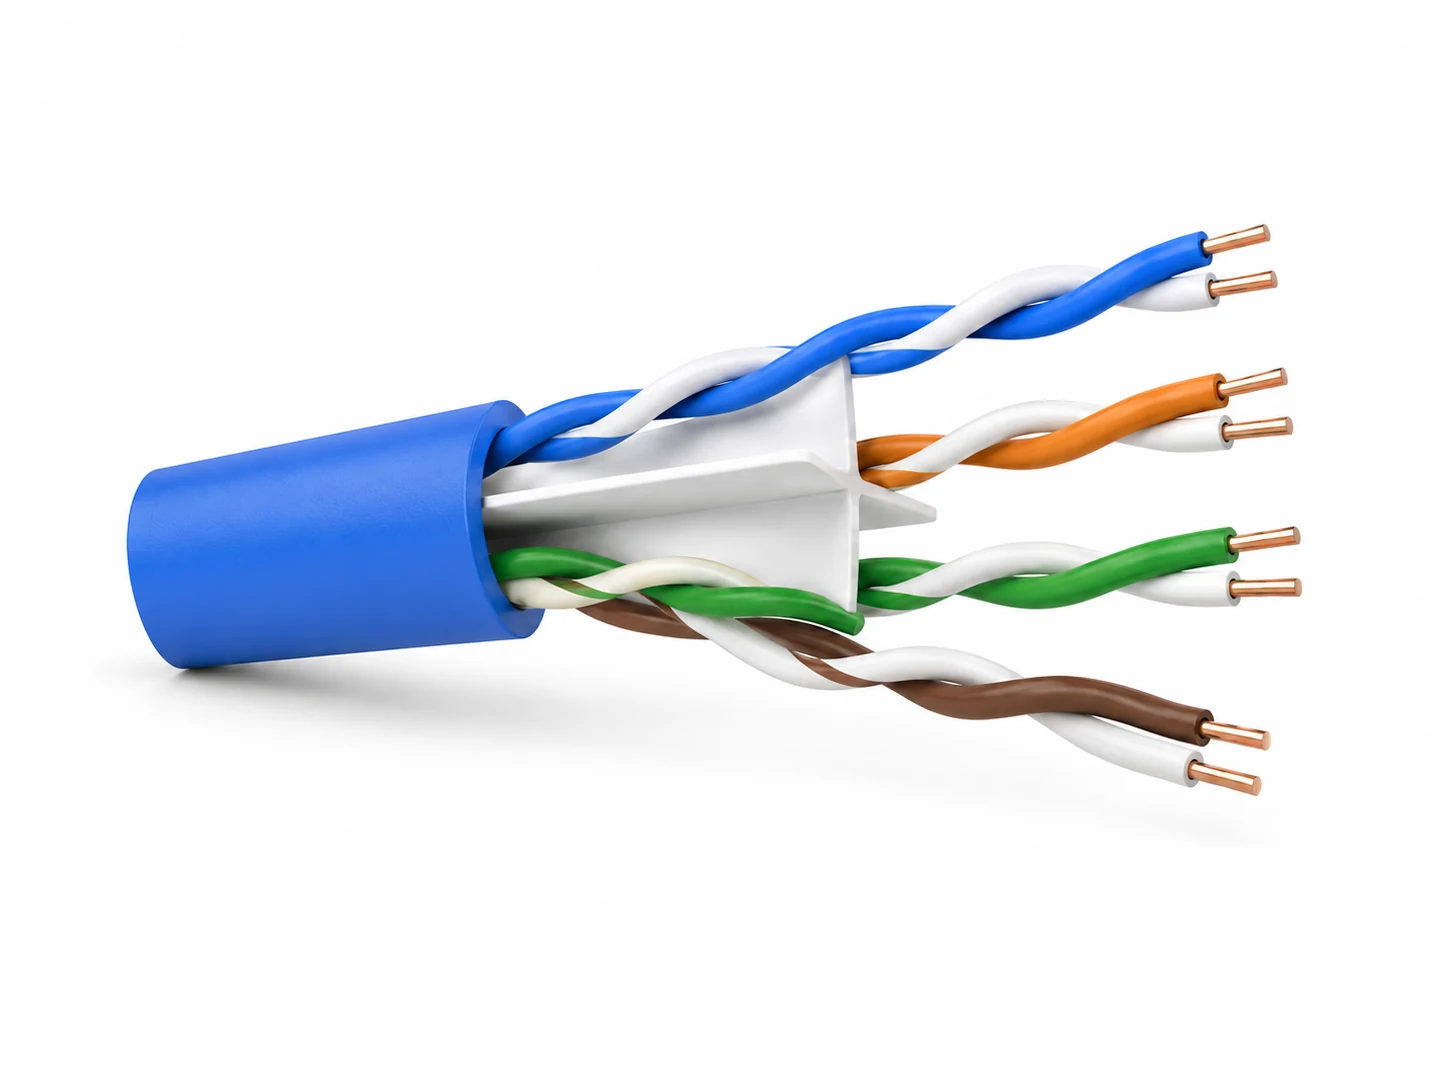
Explanatory 3D illustration, not a real test report or certification result. Retain measured pitch, concentricity and foaming degree when applicable, linked to the actual sample.
Просмотрите иллюстрацию цепочки записей в полном размере.
| Evidence layer | Responsible party | Решение, которое оно поддерживает |
|---|---|---|
| Настройка оборудования и записи процесса | Кабельный завод с участием поставщика оборудования | Может ли быть воспроизведена оцененная конструкция в заданных условиях |
| Внутренняя лабораторная предварительная проверка | Завод по производству кабелей или аккредитованная лаборатория | Готовы ли образцы к официальному представлению и на каком этапе процесс нестабилен |
| Формальная оценка и решение о сертификации | UL Solutions в рамках согласованной программы | Соответствуют ли идентифицированный продукт и площадка утвержденной области сертификации |
| Независимая проверка характеристик передачи | UL Solutions или другая указанная программа, по запросу | Соответствует ли идентифицированный кабель заявленной спецификации по характеристикам в рамках данного программы |
| Полевой испытательный тест на установленную кабельную систему | Монтажник, команда по тестированию проекта или квалифицированный специалист по обслуживанию на месте | Соответствует ли установленное соединение или канал полевым пределам проекта |
Red flags: The submission sample was made with unrecorded hand adjustments; the production BOM differs from the tested sample; a third-party report does not identify the exact construction; or the factory plans to replace compounds after approval without a documented review path.
Подготовка завода к маркировке и последующему обслуживанию
UL Listing continues after the initial evaluation. The factory must protect the approved construction, authorized labels, production records, inspection access and change-control process for as long as it produces marked cable.
UL Solutions states that the complete Listing Mark on the tag attached to the reel or smallest unit container is the proof that a particular wire or cable unit is UL Listed; surface printing is supplemental.2 The same guide says holographic labels are required for Listed communications cable and several related wire-and-cable categories. UL Solutions also explains that initial product inspection and follow-up services are part of the customer lifecycle.5
Файл готовности завода должен содержать следующую информацию:
- кто контролирует доступ к этикеткам и сверяет их использование;
- где хранятся утвержденные конструкции и макеты маркировки;
- как входящие материалы проверяются на соответствие утвержденным характеристикам;
- как производственные и инспекционные записи связаны с бухтами или коробками;
- как несоответствующие материалы и маркированная продукция разделяются;
- как инспекторы завода получают текущие записи и доступ к производству;
- как осуществляется рассмотрение изменений продукции, материалов, поставщиков, процессов, площадок или маркировки;
- как устаревшие чертежи, этикетки и производственные инструкции изымаются из обращения.
In HONGKAI’s preparation discussions, the easily missed items are raw-material traceability, retrievable production/test data and usable work instructions. Test that system before preparing the submission: ask an operator to retrieve the instruction revision used for one sample, identify its material lots and locate the corresponding raw results. A folder of disconnected screenshots does not establish that chain.
Common mistakes: The jacket print is treated as the only Listing evidence; labels can be taken without reconciliation; approved and unapproved compounds share the same internal name; or production changes are implemented before the certification owner reviews their effect.
Составьте запрос коммерческого предложения (RFQ) и матрицу ответственности на основе доказательств
The cable factory, machinery supplier, material suppliers, laboratories and UL Solutions have different responsibilities. A complete project defines the handoffs instead of asking one party to promise “UL approval.”
| Deliverable | Кабельный завод | Объем поставки оборудования HONGKAI | UL Solutions или специализированная сторона |
|---|---|---|---|
| Целевой кабель и область сертификации | Принимать решение о коммерчески реализуемом продукте и его применении | Переведите утвержденный маршрут кабеля в вопросы по оборудованию и интерфейсу | Подтвердите применимую категорию сертификации и программу оценки |
| Controlled construction and BOM | Собственные чертежи, материалы, поставщики и редакции | Подтвердите совместимость оборудования с утвержденными входными данными процесса | Проверить конструкцию в рамках официального объема проекта |
| Trial production and records | Обеспечить материалы, операторов и прослеживаемость продукции | Поддержка согласованной настройки оборудования, выходных данных FAT и технологических записей | Определяйте или фиксируйте официальные доказательства только в случае, если это предусмотрено контрактом |
| Laboratory evidence | Собственная идентификация образца и внутренние записи о выпуске | Provide agreed measurement interfaces; specialist test equipment stays separately scoped | Проводить формальную оценку или специализированные испытания под свою собственную ответственность |
| Factory control and changes | Выполняйте утвержденные процедуры, маркировку и проверку изменений | Document machine configuration and approved modifications | Провести применимую инспекцию, последующие действия и проверку сертификации |
HONGKAI can develop the overall manufacturing-equipment proposal, configure the relevant LAN stages and document agreed FAT outputs. Its own delivery responsibility is the equipment scope stated in the contract. Specialist laboratory and inspection equipment must be separately sourced and assigned; inclusion in an overall project proposal does not mean HONGKAI manufactures every instrument or acts as the certification body. Certification decisions, authorized UL markings and Follow-Up Services remain with UL Solutions under the applicable program, not with a machinery FAT.
Evidence to request: Add a certification-readiness appendix to the RFQ. It should list the target cable, product category to be confirmed, controlled materials, process route, trial samples, factory records, laboratory boundaries, label responsibility, factory-inspection preparation, change-review owner and all explicit exclusions.
Note: The strongest purchase specification does not promise that a machine will obtain UL Listing. It requires a reproducible cable route and evidence system that the factory can submit, audit and maintain under the certification body’s approved scope.
-
Обзор проводов и кабелей UL Solutions, describing communications-cable certification for CMP, CMR and CM under UL 444 and separate performance-verification services. ↩ ↩
-
UL Руководство по применению проводов и кабелей, объясняя категории продукции, знаки сертификации, Product iQ и маркировку проводов и кабелей.↩ ↩
-
Fluke Networks о тестировании каналов и постоянных линиях, что позволяет отличить полный канал от стационарной кабельной проводки и её патч-кордов.↩
-
Maillefer telecom cable insulation, иллюстрирующий сплошную/химическую пенную изоляцию и согласованные функции черчения, экструзии и измерения; не является спецификацией для оборудования HONGKAI.↩
-
UL Solutions New Client Welcome and Resources, описывающий типичный жизненный цикл от коммерческого предложения до испытаний и последующих действий, первоначальный осмотр продукции и последующие услуги.↩ ↩
 English
 हिन्दी
 فارسی