

A network-cable factory can make a reel that passes one handheld test and still lack the evidence needed to release Cat6 product consistently. Factory owners, production managers and technical buyers therefore need to decide what is being accepted: a cable design, a production lot, a third-party product listing, or an installed link.
Cat6 compliance is proved by a connected evidence chain, not by a generic “TIA certificate.” Start with the current contract standard and exact cable construction, control the geometry that creates transmission performance, test the finished cable with suitable laboratory methods, and keep lot-level records. Treat installed-link testing and independent product verification as separate evidence layers.
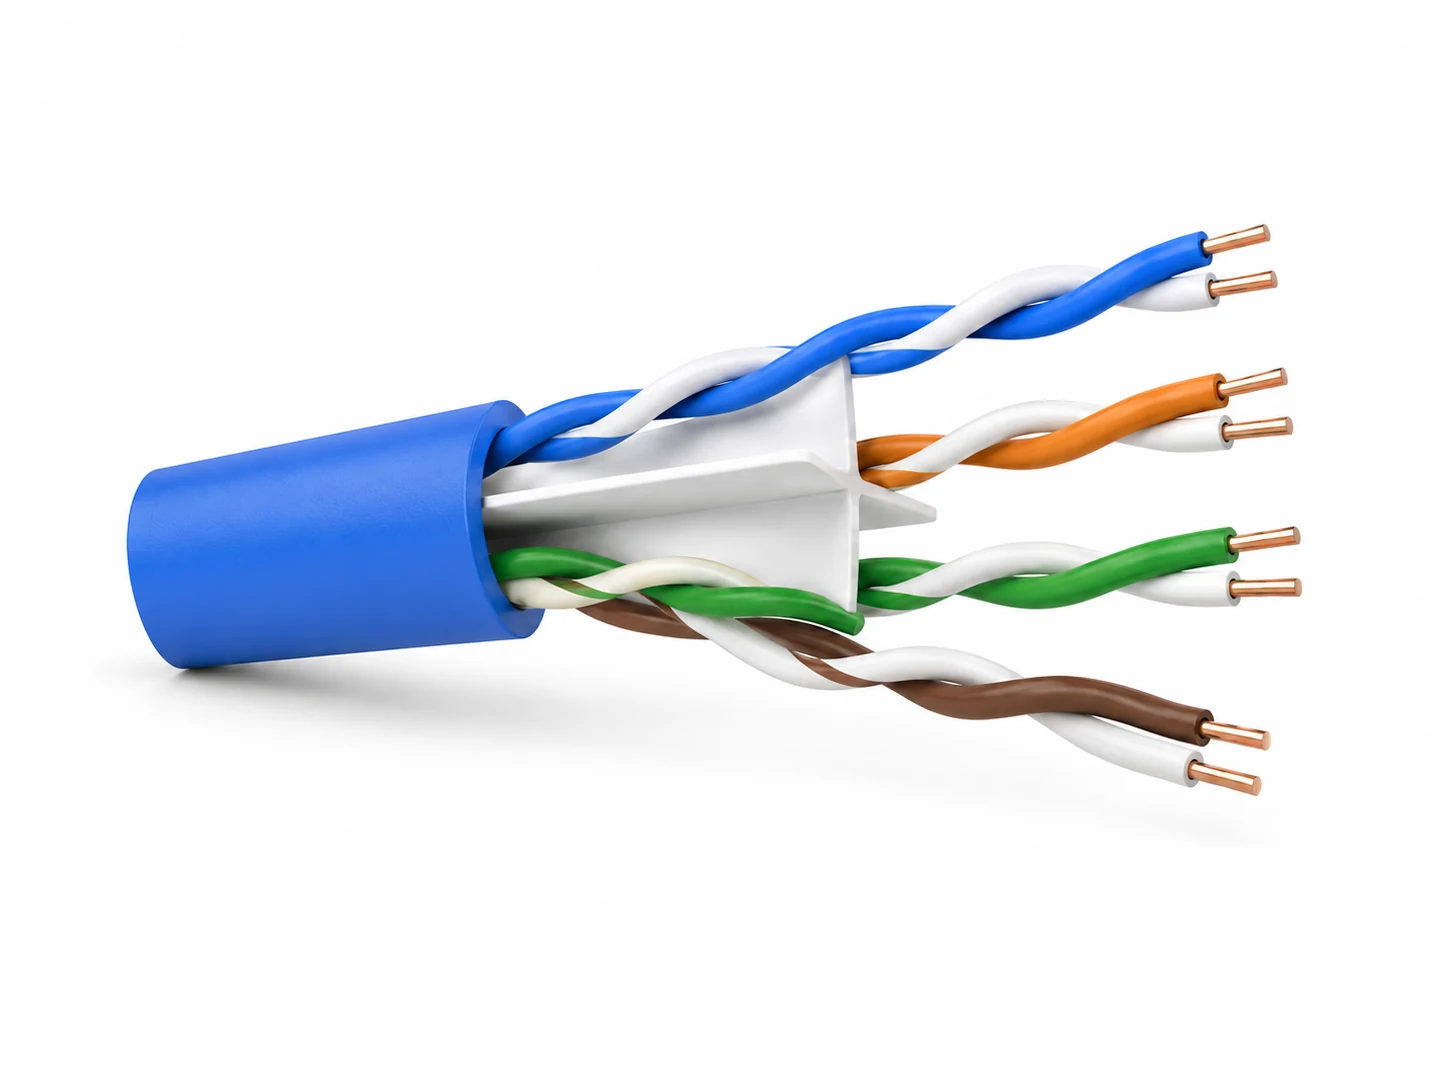
Различие имеет значение до заказа оборудования. Полный LAN cable production route must connect conductor preparation, insulation, pair twisting, cabling, optional shielding, sheathing, testing and packing. The test plan must be designed with that route because end-of-line testing can identify a result; it cannot repair uncontrolled conductor, insulation or pair geometry.
Замените “Сертификацию TIA” на именованный объект принятия
ANSI/TIA-568.2-E is a balanced twisted-pair cabling and components standard, not a universal certificate issued to every Cat6 cable factory. A buyer should name the standard edition, product construction, verification body if any, sample scope and evidence required instead of asking only for “TIA certification.”
TIA announced ANSI/TIA-568.2-E in November 2024 as the revision of ANSI/TIA-568.2-D.1 TIA also explains that its engineering committees develop standards through an ANSI-accredited process.2 Those facts establish the standards role. They do not establish that TIA has inspected a factory, tested a reel or certified a Cat6 product.
The phrase “Cat6 approval” may hide four different requests:

AI-generated explanatory illustration. Match each acceptance object to its own evidence; this is not a certificate, test result or installation drawing. View full-size illustration.
| Acceptance object | Main question | Appropriate evidence | What it does not prove alone |
|---|---|---|---|
| Cable design | Does the defined cable construction meet the signed electrical and physical requirements? | Controlled specification, qualified samples, laboratory results and change control | That every later production lot remains within control |
| Production lot or reel | Was this identified output released against the factory plan? | Traceable raw-material, process, dimensional and finished-cable records | Independent product verification or installed-link performance |
| Independent product verification | Did a named third party assess the identified product against a named specification? | Current directory entry or certificate with product, standard edition, scope and surveillance status | A different model, construction, jacket rating or unlisted factory |
| Установленное постоянное соединение или канал | Does the completed cabling system pass the project’s field limits? | Calibrated field-test report with link type, adapters, instrument and results | Factory cable qualification without the rest of the installed system |
Intertek’s ETL Verified cabling directory illustrates the third-party layer: entries are organized by company and specific product, while a certificate identifies the tested construction and referenced standard.3 One published certificate also states that verification of transmission requirements is distinct from a certification program.4 This is why a buyer should verify the exact wording, product identity, current status and surveillance arrangement rather than treating any logo as a broad Cat6 claim.
Decision criterion: Write the acceptance object as a noun before choosing the test: “bulk horizontal cable,” “patch cord,” “production reel,” “permanent link” or “channel.” If the noun changes, the fixture, limits, sample preparation and responsible party may also change.
Freeze the Cable Construction Before Selecting Tests
A Cat6 test plan begins with the saleable cable definition. Category alone is incomplete because conductor, pair, separator, shielding, jacket, installation use and delivery form change what must be manufactured and what evidence the customer may request.
The buyer should approve at least these inputs before the supplier fixes the equipment route or FAT scope:
- solid or stranded conductor and the approved conductor material;
- conductor size and finished conductor tolerance;
- insulation material, nominal dimensions and color identification;
- U/UTP, F/UTP or another defined screening construction;
- pair lay plan and any separator construction;
- cabling lay, binder or shield elements where applicable;
- материал оболочки, маркировка, цвет и требования рынка по пожарной безопасности или экологическим нормам;
- объемный кабель, патч-корд, граница приемки постоянной линии или канала;
- целевое стандартное издание, технические требования заказчика и программа третьей стороны, если требуется;
- длина бухты или коробки, длина образца, кондиционирование и план отбора проб для выпуска.
IEC 61156-5:2020 is a separate official reference for symmetrical pair/quad cables used primarily in horizontal floor wiring. Its public scope covers individually screened, common-screened and unscreened pairs or quads; the purchased standard is needed to establish the applicable detailed requirements.5 ISO/IEC 11801-1:2017, with its later amendment, addresses generic customer-premises cabling across multi-vendor systems.6 These standards are related to the product and system decision, but they are not interchangeable labels. The signed order must say which document and edition governs each acceptance object.
Common mistakes: A quotation says only “Cat6 UTP, Fluke test pass.” It does not identify bulk cable versus installed link, conductor construction, sample preparation, test method, standard edition, parameter set, limit set, instrument class or raw-data format.
Повышение производительности на этапе до финального анализатора
Cat6 electrical performance is created through repeatable conductor, insulation, twisting and cabling geometry. Final transmission testing verifies the result, while upstream process records explain why the result is stable or why it failed.
Для маршрута Cat6 UTP наиболее полезный план контроля следует физическому процессу:
| Production stage | Обработка доказательств для сохранения | Почему запись должна находиться в цепочке подтверждения |
|---|---|---|
| Подготовка проводника | Партия поставщика, идентификация материала, размер проводника и применимые данные о сопротивлении | Задает электрические и размерные параметры для изоляции |
| Изоляция токопроводящей жилы | Партия изоляции, тенденция диаметра, данные об эксцентриситете или концентричности, состояние поверхности, протокол испытания высоким напряжением и идентификация барабана | Отслеживает геометрию и целостность каждого изолированного проводника |
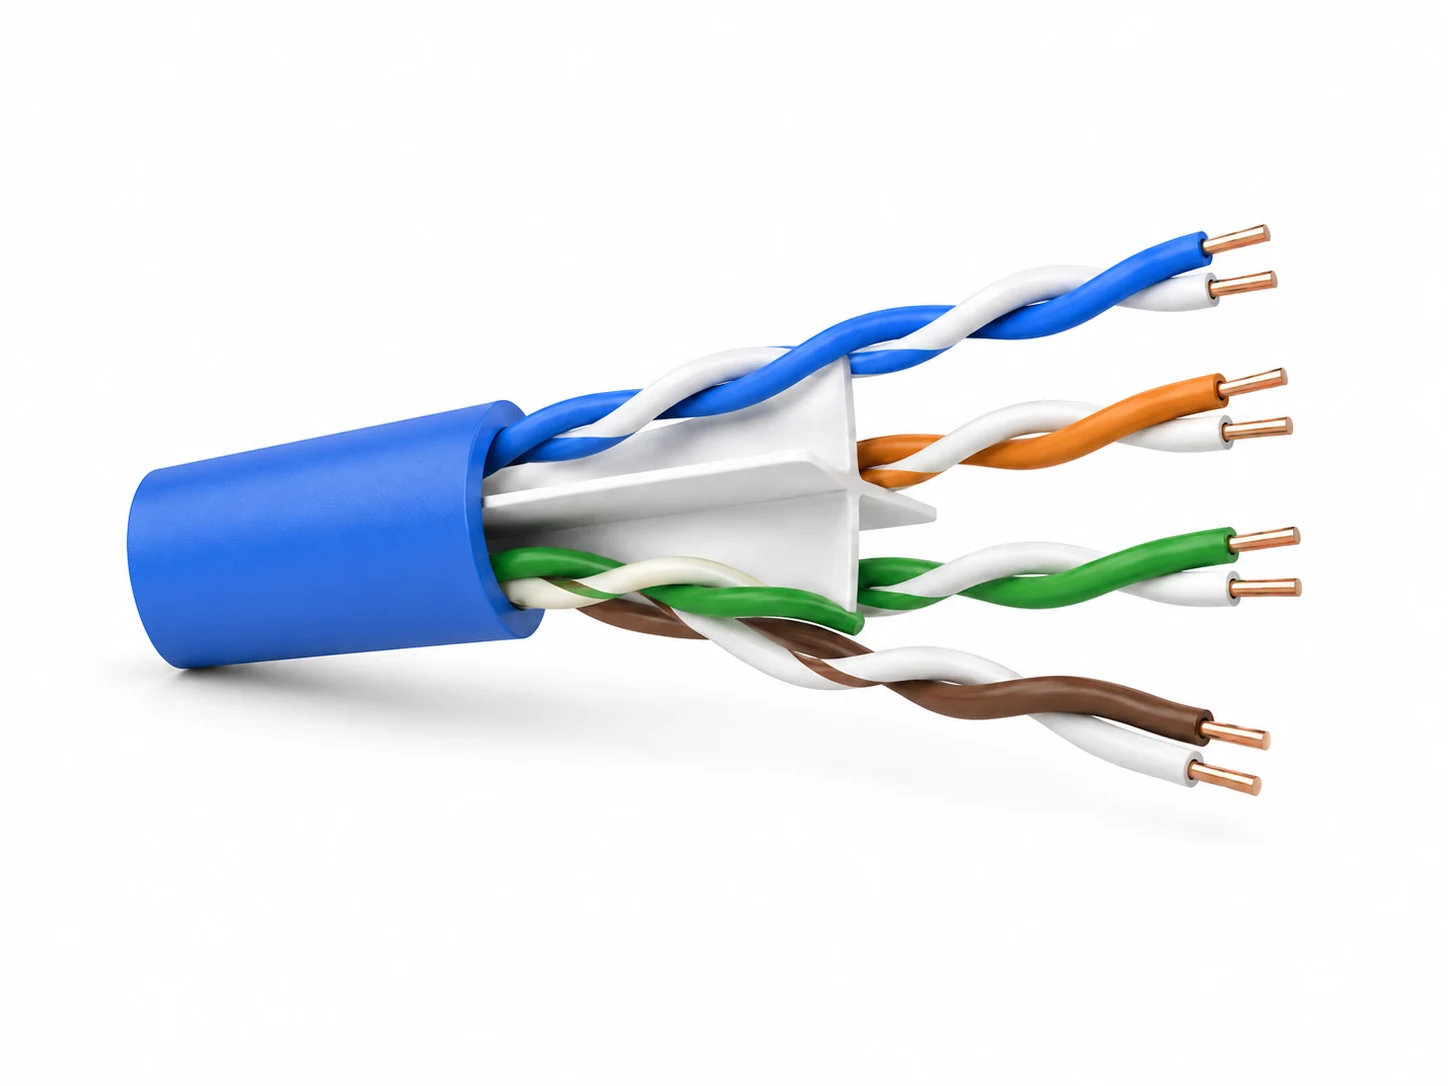
| Скручивание пар | Идентификация пары, настройка шага скрутки, настройки натяжения/обратного кручения (где применимо), схема расположения на барабане и визуальное состояние | Связывает баланс пары и повторяемость с результатом готового кабеля |
| Кабели и разделитель | Последовательность пар, шаг скрутки кабеля, идентификация разделителя, настройки натяжения и наблюдения за деформацией | Записывает геометрию, образующуюся при объединении четырёх пар в одну жилу кабеля |
| Обшивка | Партия оболочки, размеры сердечника до наложения оболочки, тенденция изменения конечного диаметра, запись маркировки/длины и бухта на приёмной катушке | Показывает, изменил ли конечный процесс сердечник или идентификацию продукта |
| Лабораторные испытания готового кабеля | Sample ID, length, conditioning, fixture, calibration status, standard/limit set, raw plots and result | Предоставляет доказательства выпуска для идентифицированной пробы и партии |
The HONGKAI LAN cable production guide maps Cat6 UTP production through insulation, precision pair twisting, separator handling where the approved construction requires it, cabling, sheathing, electrical testing and packing. That route is a project reference, not a declaration that every Cat6 design uses the same separator, machine model or acceptance limit.
How to verify: Ask the line supplier to map each critical finished-cable result back to a controllable production variable and a retained record. “The analyzer will tell us” is incomplete unless the factory can identify which process data will be checked after a failure.
Отдельные заводские лабораторные испытания и полевые испытания
Factory cable release and installed-cabling field testing answer different questions. A field tester is valuable for permanent-link or channel acceptance, but it should not automatically replace the laboratory method and fixtures needed to qualify bulk cable or components.
TIA’s ANSI/TIA-1152-A announcement defines requirements for field test instruments used with balanced twisted-pair cabling, including reporting and accuracy performance.7 That scope is useful when the acceptance object is an installed cabling configuration. A factory product program may require different laboratory instrumentation, fixtures and sample preparation to assess the cable or component itself under the governing product standard.
Используйте лестницу доказательств вместо одной общей позиции тестера:
| Evidence layer | Typical decision | Категория прибора или записи | Buyer check |
|---|---|---|---|
| Контроль в процессе | Is the manufacturing process holding the approved geometry? | Diameter/concentricity measurement, spark testing, lay/tension records and dimensional inspection | Can each reading be tied to a core, pair, reel and time window? |
| Factory electrical release | Does the identified cable sample meet the signed cable requirements? | Suitable resistance and transmission-measurement system with approved fixtures and software | Are method, calibration, sample length, conditioning and raw plots recorded? |
| Independent verification | Has the identified product been assessed by the named body? | Third-party report, directory entry and surveillance evidence | Do company, factory, model, construction and standard edition match? |
| Installation acceptance | Does the completed link or channel meet the project limit? | Полевой тестер и адаптеры для корректного соединения/канала | Is the selected limit set correct for the installed configuration? |
For machinery procurement, the HONGKAI LAN production guide identifies electrical testing as a supporting system whose scope requires written project confirmation. The buyer should separately name responsibility for the analyzer, fixtures, software, calibration service and third-party verification; those items should not be implied by the extruder, twister or cabling machine.
Note: A field PASS file is evidence for the tested configuration at the recorded time. It is not by itself evidence that every reel from the factory, every product variation or every future production lot meets the same requirements.
Fluke Testing: Is the Requirement for a 305 m Reel or a 100 m Connection?
Before accepting a requirement to “pass Fluke,” define the product being tested, its actual test length, the connection arrangement and the selected limit. A 305 m box or reel and a connection of approximately 100 m represent different customer requirements; a PASS result is useful only when the test setup matches the agreed acceptance object.
HONGKAI insight: In the customer requirements described for this guide, Fluke testing is a preferred practical acceptance reference. Some customers ask about a complete 305 m box or reel; others describe a finished connection of around 100 m. Confirm which form the customer means before discussing performance or a pass rate. These are examples of project requirements, not a universal length rule or a promised test outcome.
Use precise terms when converting the customer’s wording into the test plan. Fluke describes a conventional channel as the complete connection including patch and equipment cords, with an overall length limit of 100 m. A permanent link is the fixed portion, with a 90 m limit in that model. Testing a patch cord itself uses the relevant patch-cord limits and adapters, which assess its end connections differently from channel testing.8 Следовательно, только длина не определяет правильный режим испытаний.
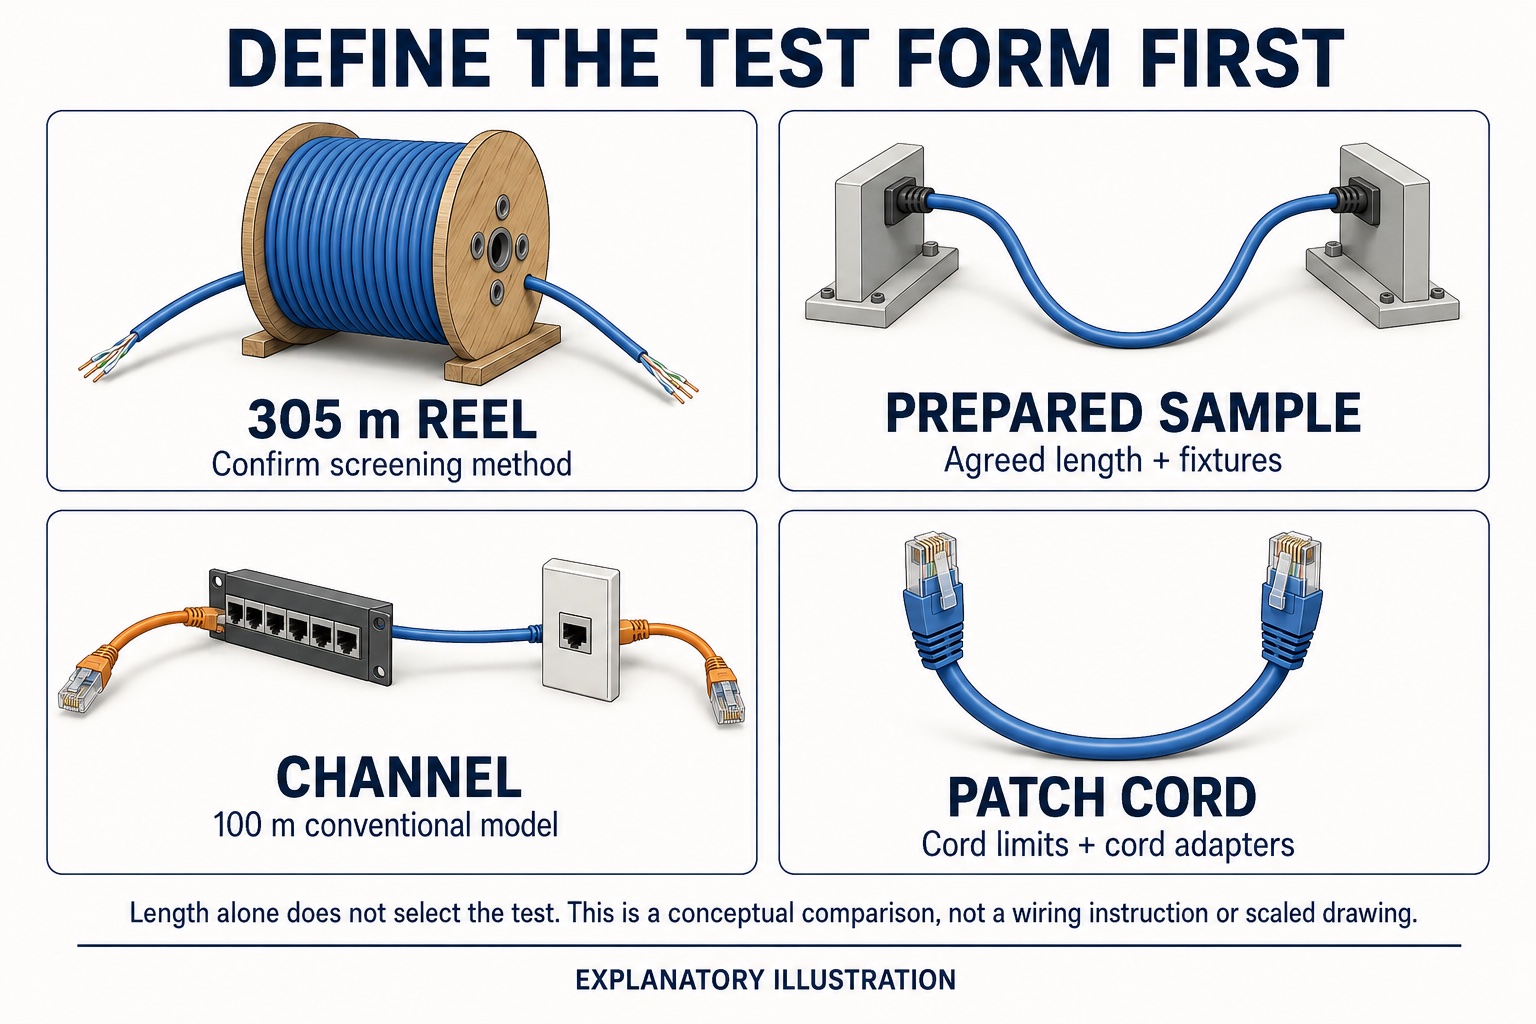
AI-generated conceptual comparison, not a wiring diagram. The 100 m figure refers to the conventional channel model, including its cords. Reel screening, prepared-sample testing and patch-cord testing require their own agreed methods and limits. View full-size illustration.
| Customer wording | Что должен уточнить покупатель | Запишите до подтверждения результата |
|---|---|---|
| “Test the 305 m box or reel” | Требуется ли экранировать кабель в бухте или проверять подготовленный образец на соответствие требованиям к компонентам? Доступны ли оба конца? | Упаковка и длина после испытаний, состояние в бухте/выпрямленное состояние, компоновка с одним концом/двумя концами, измеренные параметры и согласованный предел |
| “Test the approximately 100 m finished connection” | Является ли это каналом, подготовленным образцом кабеля или другим заданным сквозным соединением? | Схема подключения, фактическая длина, вилки/розетки, адаптеры и точное наименование предела |
| “Протестируйте патч-корд” | Имеет ли клиент в виду кабель как компонент, включая его вилки, или полный канал, содержащий этот кабель? | Cord construction and length, applicable cord test configuration and acceptance criteria |
Fluke’s single-ended DSX application note explains that reel screening measures a limited parameter set and cannot replace all double-ended measurements. It also notes that coiling can affect results and distinguishes typical 305 m reels from formal component testing based on a prepared 100 m sample with specified terminations.9 Confirm the supported method with the instrument supplier; do not select a channel limit merely to obtain a PASS for a reel.
Evidence to request: Save the Fluke model, software version, adapter identification, calibration status, test-limit name, cable/sample ID, actual length and complete result file. If the customer requests a pass rate, agree whether the denominator is boxes, reels, prepared samples or finished connections, and how first tests and retests are reported. Keep differently configured tests in separate result groups; no acceptance percentage is assumed here.
Диагностика неудачного результата по цепочке процессов
A failed Cat6 result should trigger a controlled check sequence: first verify the sample and measurement setup, then inspect the production records connected to the failure pattern, and only then adjust the process. Changing several settings at once destroys the evidence needed to confirm the cause.
Use the table as a proposed investigation record, not a confirmed diagnosis or a list of the most common causes. Each process connection must be checked against the actual cable design, raw measurements and the factory’s validated process plan; the table does not replace the governing test method.
| Семейство наблюдаемых результатов | Проверьте перед изменением производства | Участки процесса для следующего осмотра | Recovery evidence |
|---|---|---|---|
| Неожиданный результат по затуханию или вносимым потерям | Длина образца, температура проводника, соединители/оснастка, калибровка и нормализация длины | Запись о размере/материале токопроводящей жилы, соединениях, состоянии изоляции и готовой длине | Повторный результат из той же пробы плюс отдельно идентифицированная подтверждающая проба |
| Неравномерность, связанная с обратными потерями или импедансом | Оснастка, оконцевание, обращение с образцами и согласованность исходного следа | Диаметр/концентричность жилы, стабильность шага скрутки пары, натяжение при сдаче в бухту, положение разделителя и деформация, вызванная оболочкой | Стабильные исходные данные и записи размеров/технологического процесса в пределах утвержденного диапазона |
| Отказ, связанный с перекрестными помехами | Идентификация пары, сопоставление адаптера, изоляция оснастки и установка пределов | Pair lay coordination, pair balance, cross-over/sequence, separator geometry and pair deformation during cabling or jacketing | Повторяемый результат в рамках утвержденного плана отбора проб с прослеживаемыми данными по паре/процессу |
| Resistance or resistance-unbalance concern | Сопротивление контакта, подготовка образца, обнуление прибора и метод температурной коррекции | Conductor input, diameter trend, joints and pair/core identity | Corrected measurement plus conductor and sample traceability |
| Проблема задержки или синхронизации между парами | Длина образца, схема соединения пар и настройки программного обеспечения | План скрутки пар, фактические записи шага скрутки и соотношение длины пары | Подтвержденная идентичность пары и воспроизводимость измерений в соответствии с утвержденным методом |
Red flags: The only retained record is a screenshot that says PASS. It omits the raw plot, test limit, standard edition, sample ID, instrument serial number, calibration state, adapter/fixture, operator and time.
Turn Compliance into an RFQ and FAT Evidence Package
The machinery RFQ should define who supplies each production and testing function, while FAT should prove the agreed sample can be produced under recorded conditions. Product verification and continuing factory surveillance remain separate commercial and conformity-assessment scopes.
Build the RFQ package around the following inputs.
- утверждённый чертёж кабеля и график производства;
- действующие редакции стандартов и пределы, установленные заказчиком;
- каждый реализуемый вариант продукции, включенный в первый этап приемки;
- состояние поставки запланированного сырья и проводника;
- схема технологического маршрута и карта ответственности оборудования;
- требуемые встроенные измерительные приборы, испытание на искру и хранение данных;
- параметрический набор заводской лаборатории, оснастка и ответственность за программное обеспечение;
- правила отбора образцов, кондиционирования, оконечного соединения и повторных испытаний;
- for Fluke-based acceptance, the box/reel, cable-sample, patch-cord or channel boundary, exact limit and pass-rate calculation;
- Материал FAT, план отбора проб, определение стабильного режима и обязанности свидетеля;
- independent verification target, application owner and surveillance boundary;
- field-test boundary if installation acceptance is also part of the project;
- формат отчета, экспорт необработанных данных и поля прослеживаемости.
Evidence to request: For the first accepted Cat6 run, retain the material lots, machine setup, stable production window, reel map, dimensional data, sample extraction point, laboratory setup, raw results, disposition and any approved deviation in one release package.
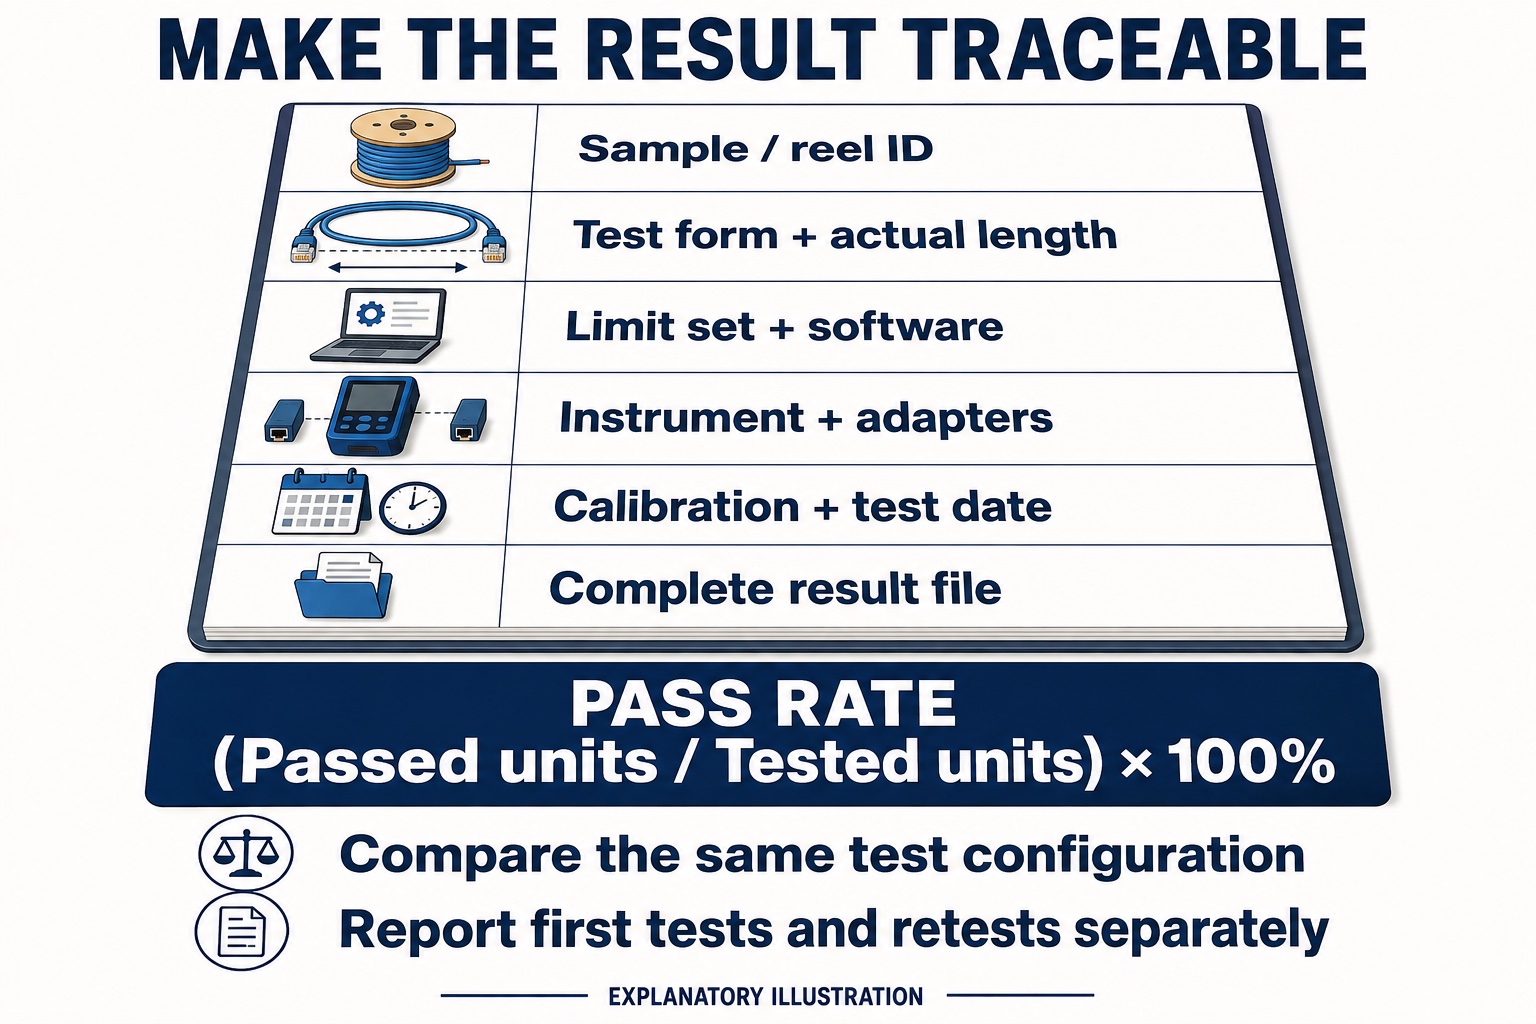
AI-generated explanatory illustration, not a real test report. Pass rate equals passed units divided by tested units, multiplied by 100%. Agree the unit, use the same test configuration within each result group, and report first tests and retests separately; no acceptance percentage is implied. View full-size illustration.
The factory should also protect change control. A different conductor, insulation grade, pair lay plan, separator, jacket compound, supplier, tooling or process window may affect the evidence basis. The responsible technical owner should decide whether the change needs a comparison trial, partial requalification, full third-party review or only a documented routine check.
The resulting release package should let the buyer trace an accepted sample back to the cable drawing, material lots, production window and test setup. Keep that evidence tied to the approved construction so a later product or process change receives an explicit technical review.
-
TIA announcement for ANSI/TIA-568.2-E, released in November 2024. ↩
-
Обзор разработки стандартов TIA, describing TIA engineering committees and the ANSI-accredited process. ↩
-
Intertek ETL Verified cabling products directory, сгруппированный по публичным компаниям и продуктам.↩
-
Intertek ETL Verified Certificate of Conformance example, used only to illustrate the scope wording of one independent verification document. ↩
-
IEC 61156-5:2020 official catalogue page, для симметричных парных/четверочных кабелей с горизонтальной укладкой на пол. ↩
-
ISO/IEC 11801-1:2017 official catalogue page, включая опубликованные поправки и исправления в течение жизненного цикла.↩
-
TIA announcement for ANSI/TIA-1152-A, описывающий требования к приборам и измерениям для полевых испытаний симметричных витых пар. ↩
-
Fluke Networks explanation of channel, permanent-link and patch-cord testing, used for test-configuration terminology; confirm the current contract edition and instrument limit library for acceptance. ↩
-
Fluke Networks: Одностороннее тестирование с анализатором кабелей DSX, explaining the limits of reel screening and its distinction from formal component testing. ↩
 English
 हिन्दी
 فارسی