

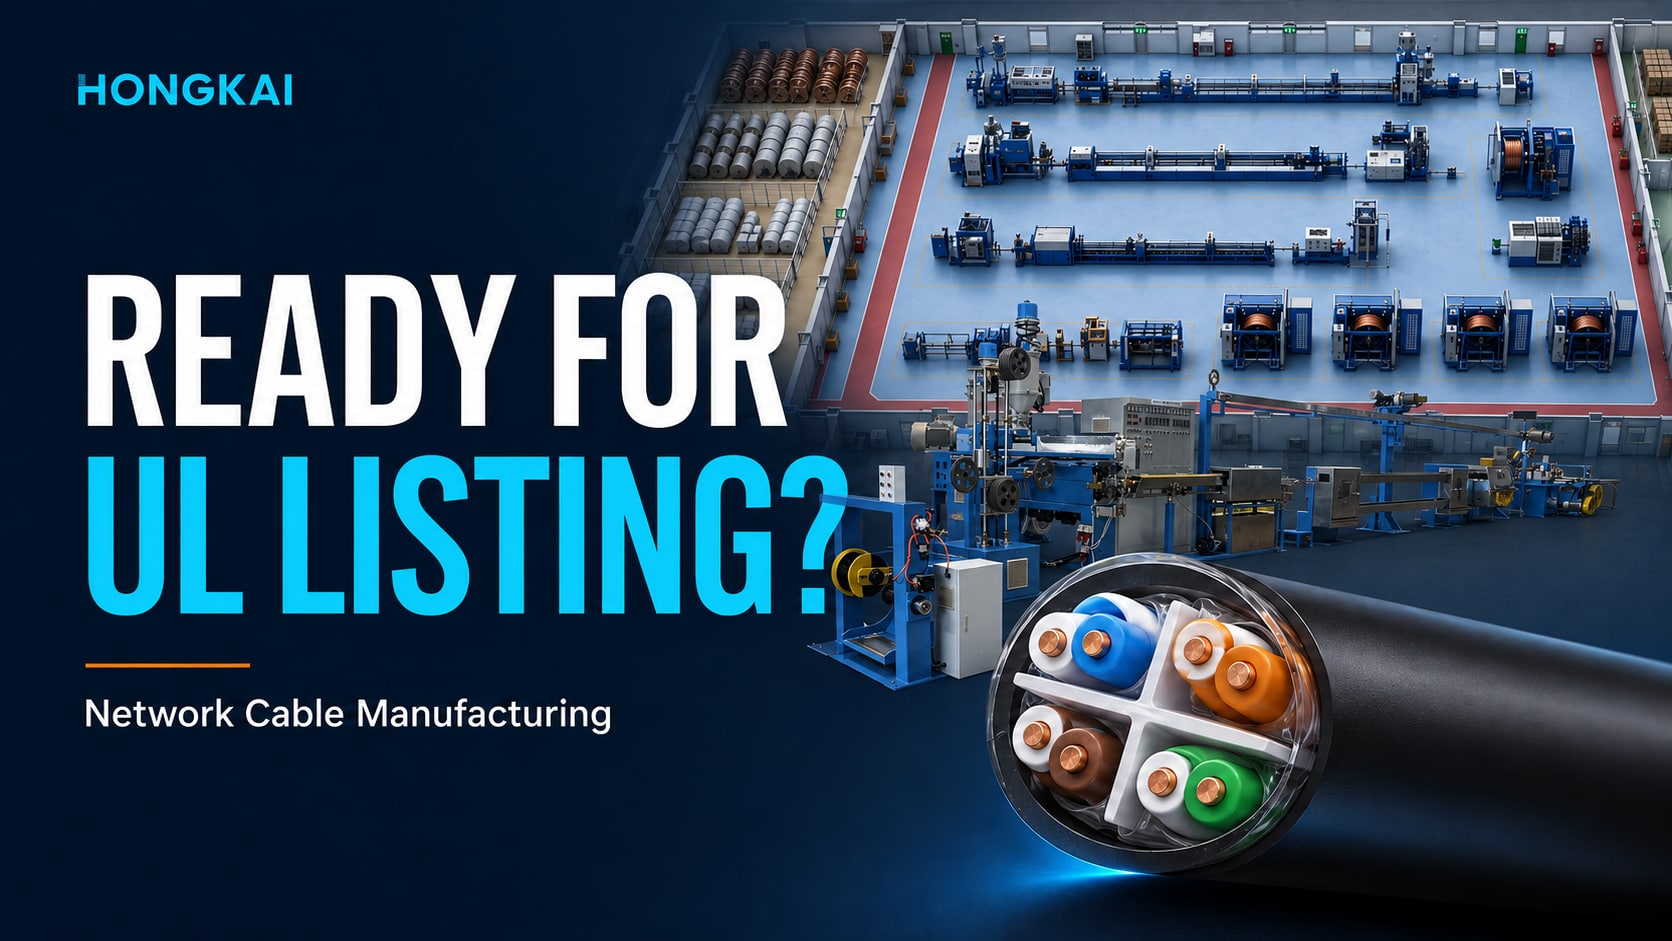
Preparing for network cable UL Listing starts with the exact cable, intended installation type, manufacturing site and certification scope, before testing becomes the main task. The practical decision is not which machine can “make a UL cable,” but which controlled product and production system will be submitted and maintained.
UL Listing is a product-and-factory control program, not a one-time machine setting or a logo added after production. A factory should freeze the construction, confirm the applicable UL category with UL Solutions, prepare representative samples and evidence, and build ongoing material, process, marking and change controls before formal evaluation.
O HONGKAI rota de produção de cabo LAN connects conductor preparation, insulation, pair twisting, cabling, optional shielding, sheathing, testing and packing. UL Solutions remains responsible for determining the applicable certification program, investigation requirements, authorized markings and follow-up obligations. HONGKAI equipment configuration and factory trials should therefore support the approved cable specification; they cannot replace the certification body’s decision.
Comece com o Objeto de Certificação Exato
The first document should name what will be certified or verified. “Cat6 with UL” is incomplete because safety Listing, transmission-performance Verification, cable assemblies and installed cabling are different objects with different evidence.
UL Solutions states that communications cable types such as CMP, CMR and CM may be certified to UL 444, while performance verification can be provided separately when required.1 Seu Guia de Aplicação de Fios e Cabos também distingue produtos Listados, Classificados, Certificados e Verificados e orienta os usuários a verificar a categoria e as marcações aplicáveis do produto.2
| Requested object | Decisão que deve ser congelada | Evidência primária após aprovação | O que a evidência não cobre automaticamente |
|---|---|---|---|
| Cabo de comunicações listado | Tipo de cabo pretendido, construção, classificações, local de fabricação e categoria aplicável | Informações da Lista Autorizada, marcações e registro atual do Product iQ | Cada outra capa, condutor, fábrica ou família de cabos |
| Cabo LAN com desempenho verificado | Especificação exata de desempenho de transmissão e construção do produto | Marca de Verificação e escopo do diretório ou certificado específico do produto | Listagem para uso em caso de incêndio ou instalação, salvo se incluída separadamente |
| Conjunto de cabo de comunicações | Construção da montagem finalizada, componentes e avaliação exigida | Evidência de Listagem ou Verificação específica da montagem | Desempenho de cabo horizontal em massa ou canal instalado |
| Link ou canal permanente instalado | Projeto do local, componentes, acabamento e limite de teste em campo | Relatório de teste de campo do projeto | Certificação de fábrica do próprio cabo |
Decision criterion: Ask the certifier to write the product category, target market, standard or program, cable type, manufacturing location, sample family and permitted marking. Keep safety Listing and performance Verification on separate lines even when the final product will carry both.
Common mistakes: A buyer asks for a “UL machine,” treats a Cat6 field-test PASS as a cable Listing, or assumes that a UL logo printed on the jacket proves current coverage. None of these defines the actual certification object.
Congele o cabo vendável antes de selecionar os testes
The factory should submit a controlled saleable construction, not a broad marketing family. The conductor, insulation system, pair design, separator or shielding, jacket compound, cable type, manufacturing site and markings all need an identified revision.
UL Solutions’ current wire-and-cable overview names CMP, CMR and CM as different communications-cable types evaluated for their intended uses.1 The target cable type affects construction and evaluation; a factory should not select a jacket only by colour, processing convenience or a supplier’s generic “UL material” description.
In HONGKAI’s equipment-scoping discussions, five questions turn “I want to make UL network cable” into a usable starting brief:
| First question | What the buyer should provide | Equipment or evidence decision |
|---|---|---|
| Is the saleable product bulk cable or a finished patch cord? | Box/reel length, conductor construction, flexibility, and whether connector assembly is included | Cable manufacture alone versus additional termination and assembly testing |
| Which constructions and categories are required now? | A drawing for each UTP, FTP, STP or SFTP request, with the exact pair/overall shield arrangement and present category range | Pair twisting, separator handling, foil wrapping, braiding and cabling route |
| What does “UL” mean in this purchase? | Target market, installation-use cable type, requested safety Listing and any separate performance Verification | Certification category and applicable test program to confirm with the certifier |
| What materials and geometry define the sample? | Conductor, insulation and jacket identities; solid or foamed insulation; dimensions and controlled drawing/BOM revisions | Extrusão, interfaces de estiramento, ferramental, controles de processo e testes de materiais |
| What must the initial line deliver, and what is only a future target? | Lançamento de produtos, variantes posteriores, saída exigida, local de fabricação e capacidade laboratorial disponível | Escopo inicial do equipamento, opções com preço separado, interfaces de teste especializadas e plano de aceitação FAT |
Bulk packaging length is not a certification category. A customer’s shorthand such as a “300 m box” or a connection “within 100 m” must be replaced by the actual ordered length and test object. A patch cord is not simply every cable shorter than 100 m: Fluke Networks distinguishes the complete channel, including cords, from the fixed permanent link.3
Likewise, commercial shield abbreviations are not enough for machine selection. The approved cross-section must show whether shielding is around each pair, around the cabled core, or both, and identify foil, braid and drain-wire details. Keep each approved variant and its proposed print legend, reel/box label, packaging, manufacturing site and subcontracted stages in the product-definition record.
A rota da máquina segue esta definição. A Rota de referência HONGKAI Cat5/Cat5e shows insulation, pair twisting, cabling, sheathing, testing and packing as a connected process, with final construction and acceptance tied to the approved specification. A Cat6 or shielded construction may change separator handling, shielding equipment, process controls and laboratory scope; no common machine list proves that all variants belong in one certification family.
What to ask: Request written confirmation from UL Solutions about the applicable category and the documents, samples and manufacturing-site information required for the proposed construction. Do this before purchasing certification labels or promising a launch date.
Emparelhar o Torcimento e a Isolação ao Construto Congelado
Pair geometry and insulation stability deserve attention before the final cable is tested. Changing the twisting route, conductor, insulation compound or foaming process after sample confirmation can change the product being submitted, even if the finished jacket still looks the same.
For pair twisting, compare the actual machine design, tension path, back-twist capability where required, payoff/take-up handling and demonstrated lay control. HONGKAI’s project experience includes triple-twist and other pair-twisting routes. For demanding constructions, Peter’s equipment-selection preference is to evaluate a suitable horizontal arrangement, but orientation alone is not proof of higher performance. Require trials on the intended conductor and insulation, agreed pitch measurements and downstream cable results before accepting a configuration.
Conductor consistency and insulation geometry are separate acceptance items. The conductor’s material, dimensions, surface condition and electrical checks should follow the product specification. For the insulating layer around each conductor, specify the compound and whether the design uses solid insulation, chemical foaming or physical foaming. Do not confuse core-wire insulation with the finished outer jacket, or assume that a familiar PVC grade is suitable for every LAN construction or cable fire rating.
Foaming is a process choice, not an automatic category upgrade or UL approval. Maillefer’s telecom-insulation documentation independently illustrates that solid and chemical-foam constructions require defined materials and line configurations, with drawing, extrusion and measurement functions coordinated as a system.4 Those examples are technical context, not HONGKAI model specifications. A HONGKAI proposal must separately confirm its compound compatibility, extrusion/foaming arrangement, tooling, concentricity control and agreed measurement provision. Moving between solid, chemical-foam and physical-foam designs requires a new compatibility and evidence review; it should not be treated as a recipe-only substitution.
Evidence to request: Freeze the conductor and compound identities, pair lay plan, insulation dimensions, concentricity definition and, for a foamed construction, the foaming-degree definition and test method. Define acceptance limits from the approved product and trial plan; do not copy a generic machine brochure value into the certification specification.
One project described by HONGKAI illustrates why the product range must precede the machine list: it covers UTP and SFTP constructions through Cat6A, with Cat7 as a later target. The discussed route combines drawing with chemical-foam insulation, triple twisting, active foil wrapping at cabling and a separately configured sheathing route. Different constructions may require different tape-handling provisions. This is a configuration example, not evidence that every variant was produced, that Cat7 was achieved, or that any product obtained UL Listing. Shielding and any protective metal-tape layer must be shown separately on the approved drawing.
Monte o Pacote de Avaliação em uma Sequência Controlada
The certification project should move from scope to construction evidence, representative samples, formal evaluation and production authorization. Individual projects vary, and UL Solutions describes the typical lifecycle as quote, testing and follow-up rather than a universal fixed timetable.5
| Sequence | Controlled output | Pergunta antes da próxima etapa |
|---|---|---|
| 01 — Scope | Tipo de cabo, mercado-alvo, local de fabricação, certificação de segurança e qualquer verificação separada de desempenho | O organismo de certificação confirmou o programa pretendido? |
| 02 — Construction | Desenho, lista de materiais (BOM), rota do processo, proposta de marcação, fornecedores e procedimento de alteração | A especificação de teste identifica a revisão da construção? |
| 03 — Evidence | Amostras representativas com registros de material, dimensionais, elétricos e de processo | Cada amostra submetida pode ser rastreada até a fabricação real? |
| 04 — Continuing control | Achados da avaliação formal, preparação da inspeção inicial e marcação autorizada/controles de acompanhamento | A fábrica está pronta para manter o escopo aprovado? |
Evidence to request: Keep the certifier’s proposal, product-category decision, sample instructions, construction description, test plan, findings, approved revisions, follow-up procedure, marking authorization and factory-inspection records under one controlled project number.
Nota: Uma amostra de pré-certificação que passa em uma verificação de laboratório interna ou externa é uma evidência técnica útil. Não constitui autorização para aplicar a Marca UL.
Conecte Cada Etapa de Produção à Conformidade Contínua
A factory needs a control plan that can reproduce the evaluated construction. The useful question for each stage is: what product characteristic is created here, what record proves control, and what change requires technical review?
The production route can be designed backward from the approved cable. The table below is a proposed control map for the factory and certifier to review; it is not a substitute for the UL Follow-Up Services procedure.
| Fase de produção | Entrada ou configuração controlada | Retained evidence | Alteração que deve acionar a revisão |
|---|---|---|---|
| Preparação do condutor | Material, construção, origem e condição do condutor acabado | Registros de identidade, lote, dimensionais e de resistência de entrada exigidos pelo plano de controle | Material, origem, revestimento ou construção do condutor |
| Isolamento do condutor interno | Composto aprovado, ferramental, diâmetro, concentricidade, cor e sistema de espumação, se utilizado | Lote do composto, configuração da linha, dados dimensionais, resultados do grau de espumação quando aplicável e registro de não conformidade | Grau do composto ou fornecedor, construção sólida/espumada, método de espumação ou ferramental |
| Torção de pares | Identidade do par, plano de torção, rota de tensão e rastreabilidade da bobina | Ficha de configuração, passo medido, ID do par/bobina e verificações em processo acordadas | Plano de enrolamento, rota da máquina ou método de controle de tensão |
| Cabeamento e blindagem | Posição do par, separador, folha metálica, fio dreno ou construção em trança | Viajante, lotes de material, geometria do núcleo e registros de continuidade, quando aplicável | Separador, material da blindagem, sobreposição, fio dreno ou design da trança |
| Revestimento e marcação | Composto de revestimento aprovado, parede, dimensão final, marcação e condição da superfície | Lote de revestimento, registro dimensional, aprovação de impressão e identificação da bobina | Tipo de revestimento ou fornecedor, tipo de cabo, classificação ou inscrição |
| Teste final e embalagem | Amostra definida, método, fonte de aceitação e rótulo da embalagem | Resultados brutos, disposição, rastreabilidade de carretel/caixa e controle de etiquetas | Método de teste, base da amostra, limite do software, embalagem ou conteúdo do rótulo |
The earlier Guia de conformidade de fábrica Cat6 explains why a final analyzer cannot repair uncontrolled conductor, insulation or pair geometry. The same logic matters here: certification evidence must be linked to the process that made the sample and to the production records that will continue after approval.
How to verify: Select one finished reel or box and trace it backward to the approved construction, material lots, process records, inspection results, final test and authorized label. Then select one material or process change and show who decides whether certification review is required before production resumes.
Separar as Verificações Pré-fabricação das Decisões da UL
Factory and third-party prechecks reduce avoidable risk, but UL Solutions controls the formal investigation scope, sample requirements, acceptance decision and authorization to use its Mark. The factory laboratory should support the submission without describing itself as the certifier.
Before formal evaluation, the factory can check whether the proposed construction is stable enough to submit. Useful preparation may include dimensional checks, conductor and insulation records, electrical prechecks, fire-test preparation by an appropriate laboratory, marking review and repeat builds from more than one production run. The exact method, equipment, sample count and pass/fail source must come from the agreed certification plan and applicable requirements.
For the equipment FAT, HONGKAI’s practical record priorities are measured pair lay/pitch, insulation concentricity and foaming degree whenever foamed insulation is used. Do not replace the last item with an operator’s observation that the insulation “looks foamed.” Agree the measurement definition, method, instrument and sampling locations before the trial, then retain actual results, units, acceptance source, instrument identity, operator/date and disposition.
Link these records to the drawing revision, machine setup, conductor and compound lots, trial reel and retained sample IDs. Record the trial conditions actually demonstrated; one successful sample is not evidence of an untested speed, material or product range. These FAT measurements support sample preparation and repeatability, but they are not a complete UL test program.

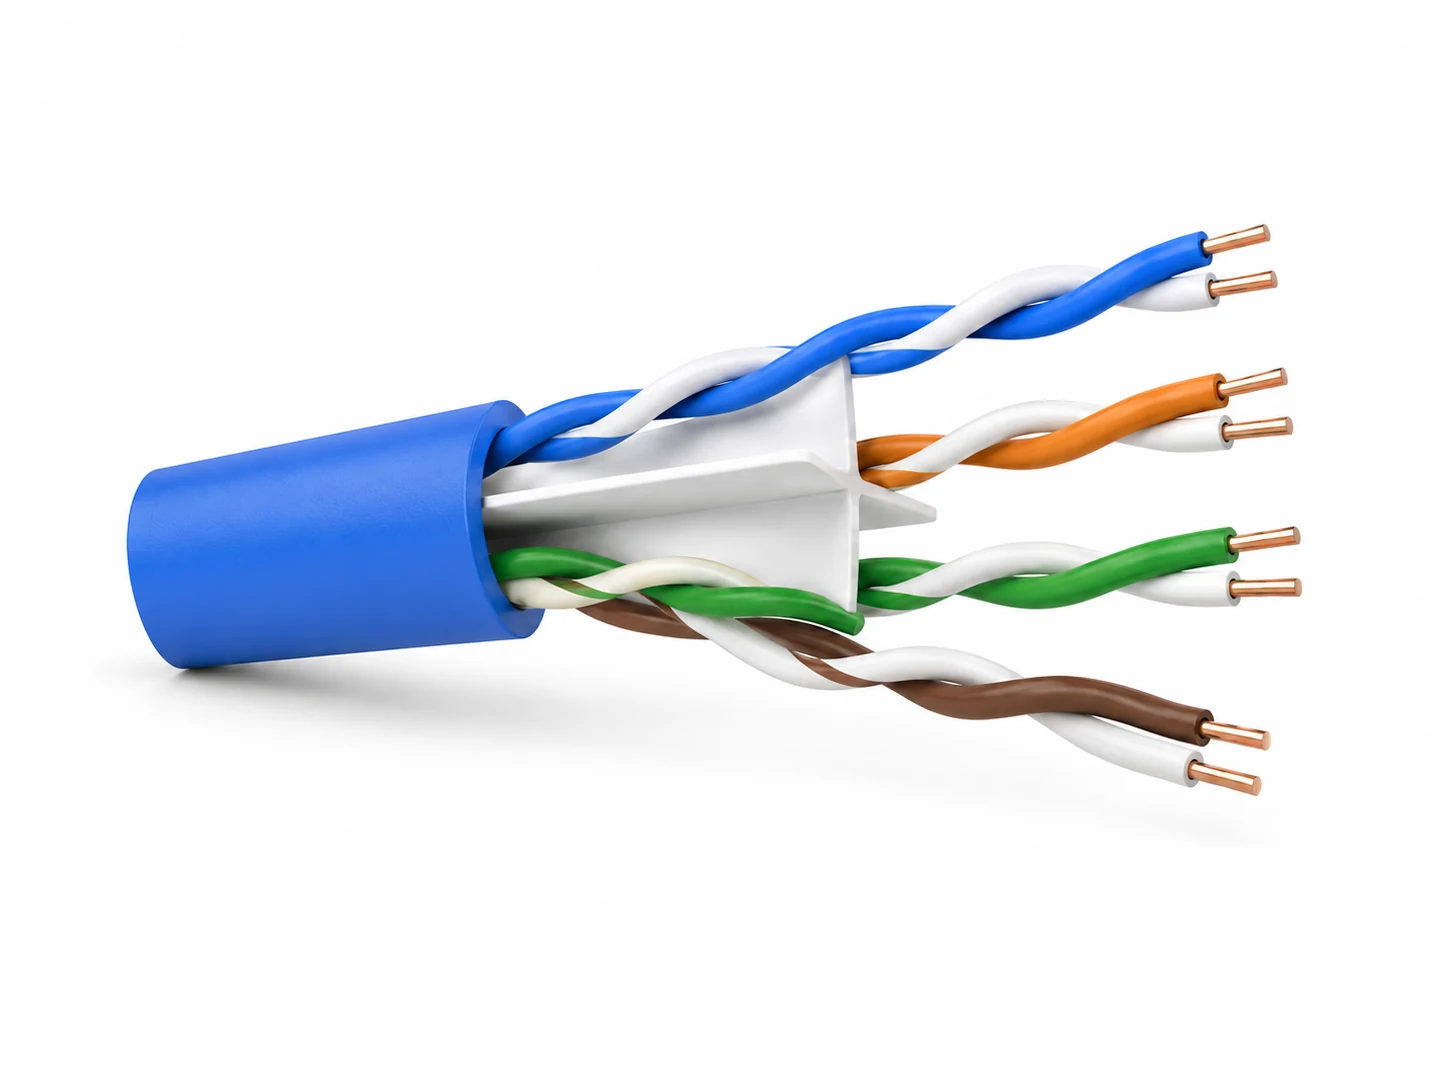
Explanatory 3D illustration, not a real test report or certification result. Retain measured pitch, concentricity and foaming degree when applicable, linked to the actual sample.
Veja a ilustração completa da cadeia de registros.
| Evidence layer | Responsible party | Decisão que apoia |
|---|---|---|
| Registros de configuração da máquina e em processo | Fábrica de cabos com contribuição do fornecedor de equipamentos | Se a construção avaliada pode ser reproduzida em condições definidas |
| Pré-verificação interna do laboratório | Fábrica de cabos ou laboratório qualificado | Se as amostras parecem prontas para submissão formal e onde o processo é instável |
| Avaliação formal e decisão de certificação | UL Solutions sob o programa acordado | Se o produto e o local identificados se qualificam para o escopo de certificação autorizado |
| Verificação independente do desempenho de transmissão | UL Solutions ou outro programa nomeado, quando solicitado | Se o cabo identificado atende à especificação de desempenho mencionada dentro do escopo desse programa |
| Teste de campo da cablagem instalada | Instalador, equipe de teste do projeto ou serviço de campo qualificado | Se o enlace ou canal instalado atende aos limites de campo do projeto |
Red flags: The submission sample was made with unrecorded hand adjustments; the production BOM differs from the tested sample; a third-party report does not identify the exact construction; or the factory plans to replace compounds after approval without a documented review path.
Preparar a fábrica para marcação e serviços de acompanhamento
UL Listing continues after the initial evaluation. The factory must protect the approved construction, authorized labels, production records, inspection access and change-control process for as long as it produces marked cable.
UL Solutions states that the complete Listing Mark on the tag attached to the reel or smallest unit container is the proof that a particular wire or cable unit is UL Listed; surface printing is supplemental.2 The same guide says holographic labels are required for Listed communications cable and several related wire-and-cable categories. UL Solutions also explains that initial product inspection and follow-up services are part of the customer lifecycle.5
O arquivo de prontidão da fábrica deve identificar:
- quem controla o acesso às etiquetas e reconcilia o uso;
- where approved constructions and marking artwork are stored;
- como os materiais recebidos são verificados em relação às identidades aprovadas;
- how production and inspection records are linked to reels or boxes;
- como o material não conforme e o produto marcado são segregados;
- how factory inspectors receive current records and production access;
- como as alterações de produto, material, fornecedor, processo, local ou marcação são analisadas;
- como os desenhos, rótulos e instruções de trabalho obsoletos são retirados de uso.
In HONGKAI’s preparation discussions, the easily missed items are raw-material traceability, retrievable production/test data and usable work instructions. Test that system before preparing the submission: ask an operator to retrieve the instruction revision used for one sample, identify its material lots and locate the corresponding raw results. A folder of disconnected screenshots does not establish that chain.
Common mistakes: The jacket print is treated as the only Listing evidence; labels can be taken without reconciliation; approved and unapproved compounds share the same internal name; or production changes are implemented before the certification owner reviews their effect.
Write the RFQ and Responsibility Matrix Around Evidence
The cable factory, machinery supplier, material suppliers, laboratories and UL Solutions have different responsibilities. A complete project defines the handoffs instead of asking one party to promise “UL approval.”
| Deliverable | Fábrica de cabos | Escopo dos equipamentos HONGKAI | UL Solutions ou parte especializada |
|---|---|---|---|
| Escopo do cabo alvo e da certificação | Assumir a decisão e a aplicação do produto comercializável | Translate the approved cable route into equipment and interface questions | Confirmar a categoria de certificação aplicável e o programa de avaliação |
| Controlled construction and BOM | Desenhos próprios, materiais, fornecedores e revisões | Confirmar a compatibilidade da máquina com as entradas do processo assinadas | Review construction within the formal project scope |
| Trial production and records | Fornecer materiais, operadores e rastreabilidade do produto | Apoiar a configuração acordada da máquina, os resultados do FAT e os registros do processo | Define or witness formal evidence only when contracted to do so |
| Laboratory evidence | Identidade da própria amostra e registros internos de liberação | Provide agreed measurement interfaces; specialist test equipment stays separately scoped | Realizar avaliação formal ou testes especializados sob sua própria responsabilidade |
| Controle e alterações de fábrica | Operate approved procedures, labels and change review | Documentar a configuração da máquina e as modificações aprovadas | Realizar a inspeção aplicável, o acompanhamento e a revisão da certificação |
HONGKAI can develop the overall manufacturing-equipment proposal, configure the relevant LAN stages and document agreed FAT outputs. Its own delivery responsibility is the equipment scope stated in the contract. Specialist laboratory and inspection equipment must be separately sourced and assigned; inclusion in an overall project proposal does not mean HONGKAI manufactures every instrument or acts as the certification body. Certification decisions, authorized UL markings and Follow-Up Services remain with UL Solutions under the applicable program, not with a machinery FAT.
Evidence to request: Add a certification-readiness appendix to the RFQ. It should list the target cable, product category to be confirmed, controlled materials, process route, trial samples, factory records, laboratory boundaries, label responsibility, factory-inspection preparation, change-review owner and all explicit exclusions.
Note: The strongest purchase specification does not promise that a machine will obtain UL Listing. It requires a reproducible cable route and evidence system that the factory can submit, audit and maintain under the certification body’s approved scope.
-
Visão geral de fios e cabos da UL Solutions, describing communications-cable certification for CMP, CMR and CM under UL 444 and separate performance-verification services. ↩ ↩
-
UL Solutions Guia de Aplicação de Fios e Cabos, explicando categorias de produtos, marcas de certificação, Product iQ e evidências de marcação de fios e cabos.↩ ↩
-
Fluke Networks sobre testes de canal e enlaces permanentes, distinguindo o canal completo da cablagem fixa e dos seus cabos de ligação.↩
-
Isolamento de cabos de telecomunicações Maillefer, illustrating solid/chemical-foam insulation and coordinated drawing, extrusion and measurement functions; not a specification for HONGKAI equipment. ↩
-
Boas-vindas da UL Solutions a Novos Clientes e Recursos, describing the typical quote-to-testing-to-follow-up lifecycle, initial product inspection and Follow-Up Services. ↩ ↩
 English
 हिन्दी
 فارسی