


A buyer planning an MPO cable manufacturing process has one central decision. Can the proposed scope release the finished assembly with every channel identified and tested? That decision is broader than choosing a polishing machine.
A complete project links two systems. The GJFJV-type cable route makes and bundles the individual tight-buffered fibers. The MPO workcell then separates, orders and loads them into the ferrule. Both the base cable and the finished assembly need their own release evidence.

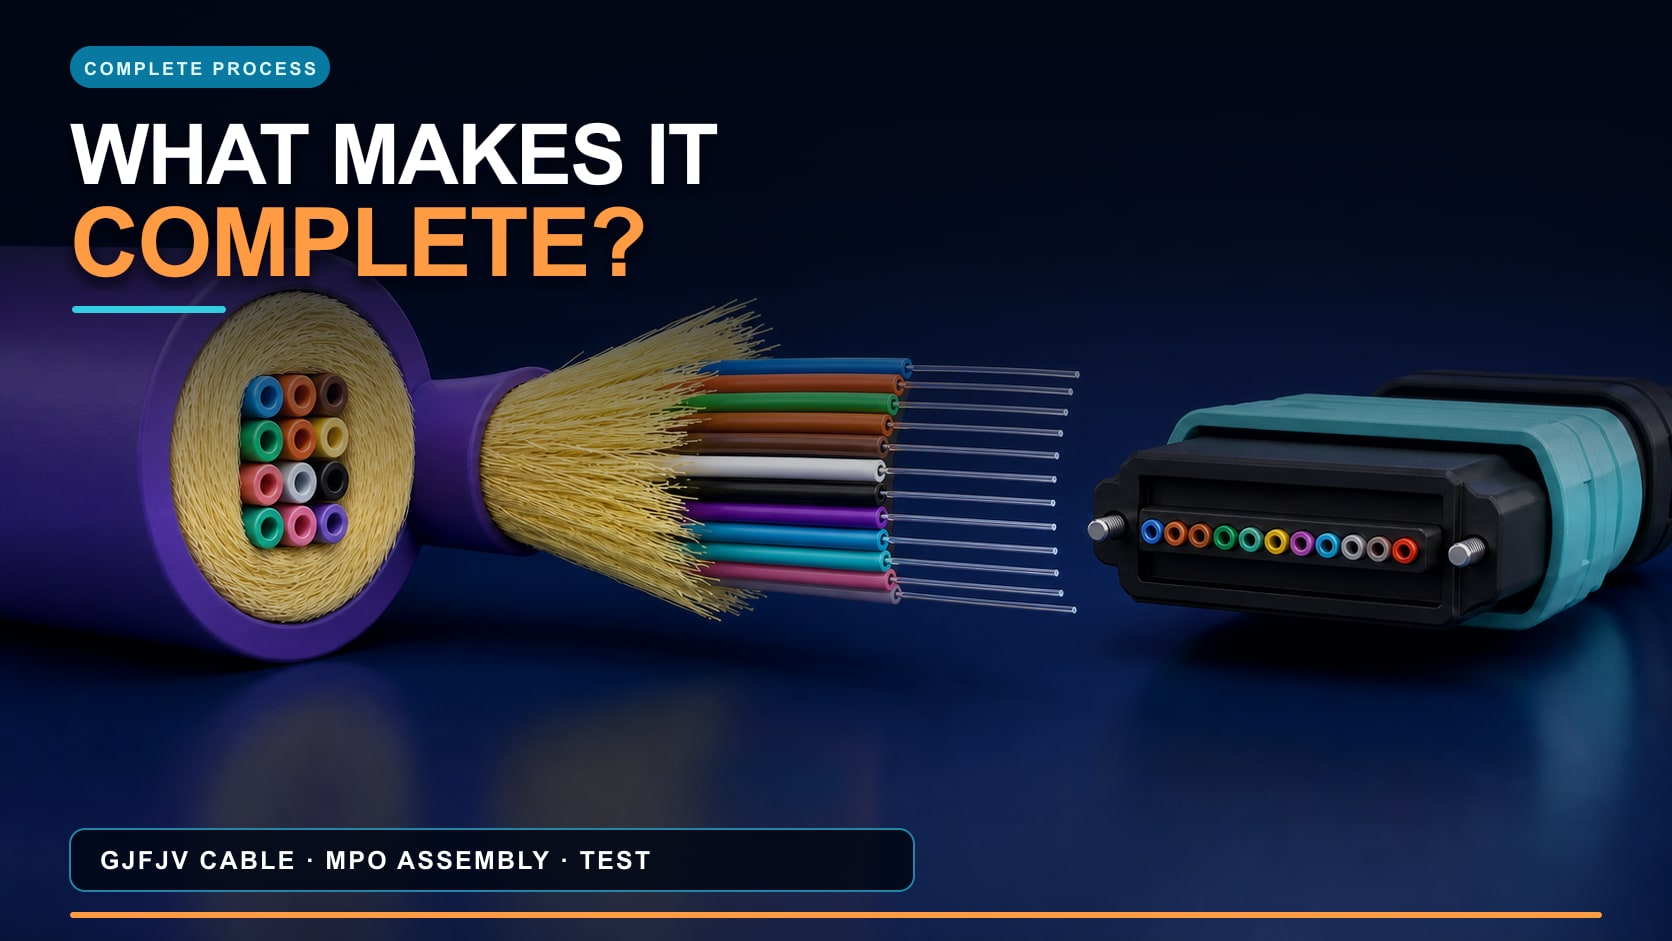
Verified-structure 3D reference: this 12-core GJFJV example has a bundled core. The ordered row is formed during ferrule preparation; the signed product drawing controls the saleable construction.
This distinction matters because MPO is a connector interface, not a universal cable construction. The project in this guide uses an indoor multi-core GJFJV-type tight-buffer cable as the reference input. A different launch cable, ferrule family, polarity or optical specification can change the machines, fixtures, test paths and FAT sample.
Untuk alur kerja konektor serat tunggal konvensional, lihat panduan produksi kabel patch serat optik. Rute tersebut bukan daftar peralatan untuk workcell MPO ini.
Ruang Lingkup untuk Dibekukan Sebelum Memberikan Penawaran untuk Jalur Lengkap
Freeze the finished assembly, base-cable drawing and release evidence before choosing equipment. An “MPO line” quotation is incomplete without the cable construction, fiber count, connector interface, key orientation, polarity, polish, optical method and traceability unit. These inputs determine the cable-line configuration and the back-end fixtures.
IEC 60794-2-23:2024 addresses indoor multi-fiber cables used in MPO-terminated assemblies. IEC 61754-7-1:2014 Dan IEC 61754-7-2:2017 cover one-row and two-row MPO interface variants. These publications help define the relevant product and interface layers. The buyer still has to approve the cable drawing, materials, process route and acceptance limits.
| Input to freeze | Keputusan pembeli | Equipment consequence |
|---|---|---|
| Finished product | Named assembly, length and branch format | Cutting, stripping, handling, labeling and test access |
| Konstruksi kabel | Fiber count, tight-buffer arrangement, aramid system and jacket | Payoffs, gathering, extrusion tooling, guides and take-up |
| Connector system | Ferrule row, gender, key orientation, housing and polish | Loading and cure holders, polishing fixture and test adapters |
| Fiber and channel map | Fiber category, count, position map and end-to-end polarity | Array fixture, work instruction, polarity tester and data fields |
| Cable acceptance | Dimensions, optical and mechanical requirements, methods and sampling | Online gauges plus separately scoped cable-laboratory equipment |
| Assembly acceptance | End-face, geometry when required, polarity and optical requirements | Inspector, interferometer when required, channel tester and data system |
| Traceability unit | Reel, cut length, connector pair, component lots and traveler identity | Barcode or traveler fields, data export and rework history |
In this guide, the launch product is the signed assembly used to prove the purchased route. A traveler is the linked production record that follows that assembly. Factory acceptance testing (FAT) must connect the launch product, traveler and raw result files.
Decision criterion: This guide uses a Make–Map–Prove–Trace test for quotation completeness. Make the signed base cable. Map every fixture, adapter and software path to the launch product. Prove cable release and finished-assembly release at separate gates. Trace each tested channel back to its source reel, components and process records. If any step lacks named equipment, method or retained evidence, the quoted scope is not yet complete. Approve expansion only for named future products.
GJFJV Cable Making in Two Manufacturing Phases
The verified HONGKAI reference has two manufacturing phases. HK-30 makes the individual tight-buffered fibers. The configured GJFJV phase gathers them, applies the aramid system and extrudes the common jacket. The quotation must state whether the gathering cage is integrated with HK-50 or supplied as a matched unit.
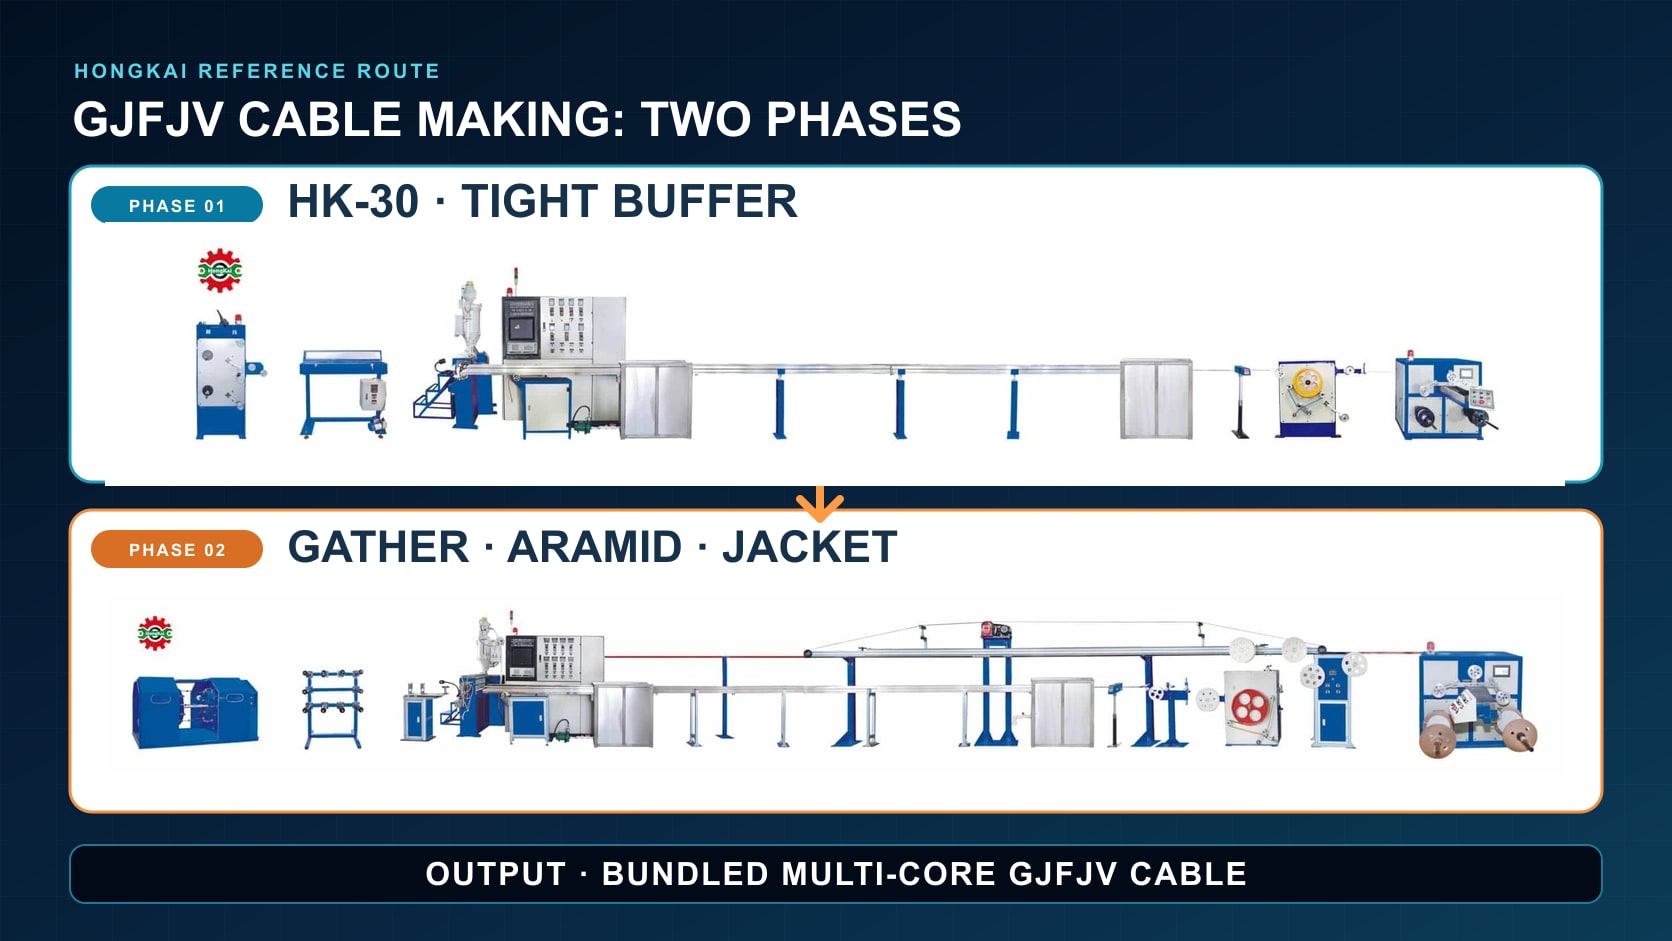
HONGKAI reference route: tight buffering, multi-fiber gathering, aramid application and common-jacket extrusion. The signed project controls the final station arrangement.
Four stages in the GJFJV cable route
-
Tight buffer — Protect each fiber. Lepaskan serat yang telah diidentifikasi, aplikasikan pelapis ketat (tight buffer), dinginkan, periksa dimensi yang diperlukan, lalu gulung serat berpelapis tersebut.
-
Gather fibers — Create the cable core. Masukkan serat ber-buffer ketat yang telah diidentifikasi ke dalam sistem pengumpul yang dikonfigurasi. Bentuk inti bundel seperti yang ditunjukkan pada gambar kabel.
-
Add the strength system — Apply aramid yarn. Rutekan benang aramid yang ditentukan di bawah tegangan terkendali. Arahkan serat dan benang ke dalam perkakas jaket.
-
Jacket and reel — Finish the base cable. Ekstrusi dan dinginkan jaket umum. Periksa dimensi yang diperlukan dan gulung reel jadi yang dapat dilacak.
Itu HONGKAI GJFJV production-line page shows the HK-30 tight-buffer phase and an HK-50 reference line. The visible functions include fiber gathering, aramid payoff, jacket extrusion, cooling, diameter measurement, capstan and take-up. This is configuration evidence, not a universal fiber count, material, speed or layout.
Data tahap kabel yang tidak boleh ditunda hingga perakitan akhir
Online diameter display is useful, but one screen value is not a complete cable release. The quotation should state which data are displayed, stored or checked offline and which laboratory instruments are included.
| Control point | Catatan untuk disimpan | Peralatan terpisah atau keputusan untuk lingkup |
|---|---|---|
| Serat optik masuk | Identitas gulungan, spesifikasi serat yang disetujui, dan bukti dasar | Metode optik masuk dan rencana pengambilan sampel |
| Fase buffer ketat | Lot material, identitas serat, pengaturan proses, alarm, dan dimensi yang diukur | Metode dimensi atau konsentrisitas offline bila diperlukan |
| Fase pengumpulan dan jaket | Identitas gulungan serat ber-buffer, lot aramid dan jaket, pengaturan jalur, alarm, dan bukti diameter | Opsi pencatatan data dan pengukuran penampang lintang offline |
| Gulungan kabel jadi | Panjang/identitas gulungan, pelepasan visual dan dimensi, kontinuitas, serta hasil optik yang disepakati | Instrumen uji optik, metode referensi, dan format catatan |
| Cable qualification | Hasil yang dipersyaratkan oleh spesifikasi kabel yang telah disetujui | Tensile, crush, bend, temperature or other project-specific laboratory equipment |
Common mistakes: A buyer budgets only the extrusion line because it includes a diameter gauge. Optical and mechanical release tests then remain undefined. A later MPO result cannot replace the base cable’s own acceptance record.
The supplier quotation reviewed for this article contains no cable-making or cable-laboratory equipment. Those items must be added to the complete-project scope rather than inferred from the back-end equipment list.
Complete Back-End Equipment Flow for MPO Assembly
The GJFJV cable brings a bundle of individual tight-buffered fibers into this workcell. The linear row is formed only during connector assembly. A signed channel map—the position-to-position drawing for both connector ends—controls fiber order and polarity.
The supplier quotation identifies equipment for array preparation, adhesive handling, cure, polish, inspection and test. It does not establish the production sequence or process settings. The signed bill of materials, connector instruction and release plan must do that.
The evidence boundary is explicit. The public HONGKAI GJFJV page supports cable-line functions. The supplied MPO catalog and quotation support equipment categories and source geometry. The cited IEC publications support interface and test-method layers. None of these sources establishes a universal recipe, throughput, acceptance limit, certification or customer result. The source-backed 3D images preserve the catalog structures while supplier brands, model text, prices and commercial terms remain excluded.
Four stages from cable end to released assembly
-
Prepare and identify — Expose and order every fiber. Open the cable end without losing fiber identity. Arrange every fiber against the signed channel map.
-
Load and stabilize — Use the qualified adhesive and ferrule route. Prepare the specified adhesive. Load the fibers and ferrule in the validated product-specific sequence.
-
Finish the ferrule — Cure, prepare, polish and inspect. Cure and prepare the ferrule, then run the multi-stage polish. Assemble the hardware at the connector-defined point and inspect the cleaned end face.
-
Verify and release — Confirm geometry, mapping and optics. Measure geometry when required. Verify the channel map and optical results before releasing the linked record package.
For the launch project, each equipment item is mapped to one of three scope labels. Diperlukan means required for this launch route, not for every MPO design. Conditional equipment enters only when the signed process calls for it.
Rework equipment stays outside normal production unless an authorized instruction allows its use. This project-specific mapping prevents optional or rework tools from becoming a false universal line. During FAT, run each applicable item with the launch product and keep the device-specific proof named below.
Persiapkan dan identifikasi serat-serat tersebut
Daftar yang dikutip dimulai dari persiapan array. Seluruh workcell juga memerlukan pengukuran dan pemotongan kabel, pengupasan jaket, persiapan aramid, serta pemuatan komponen yang diperlukan sebelumnya.
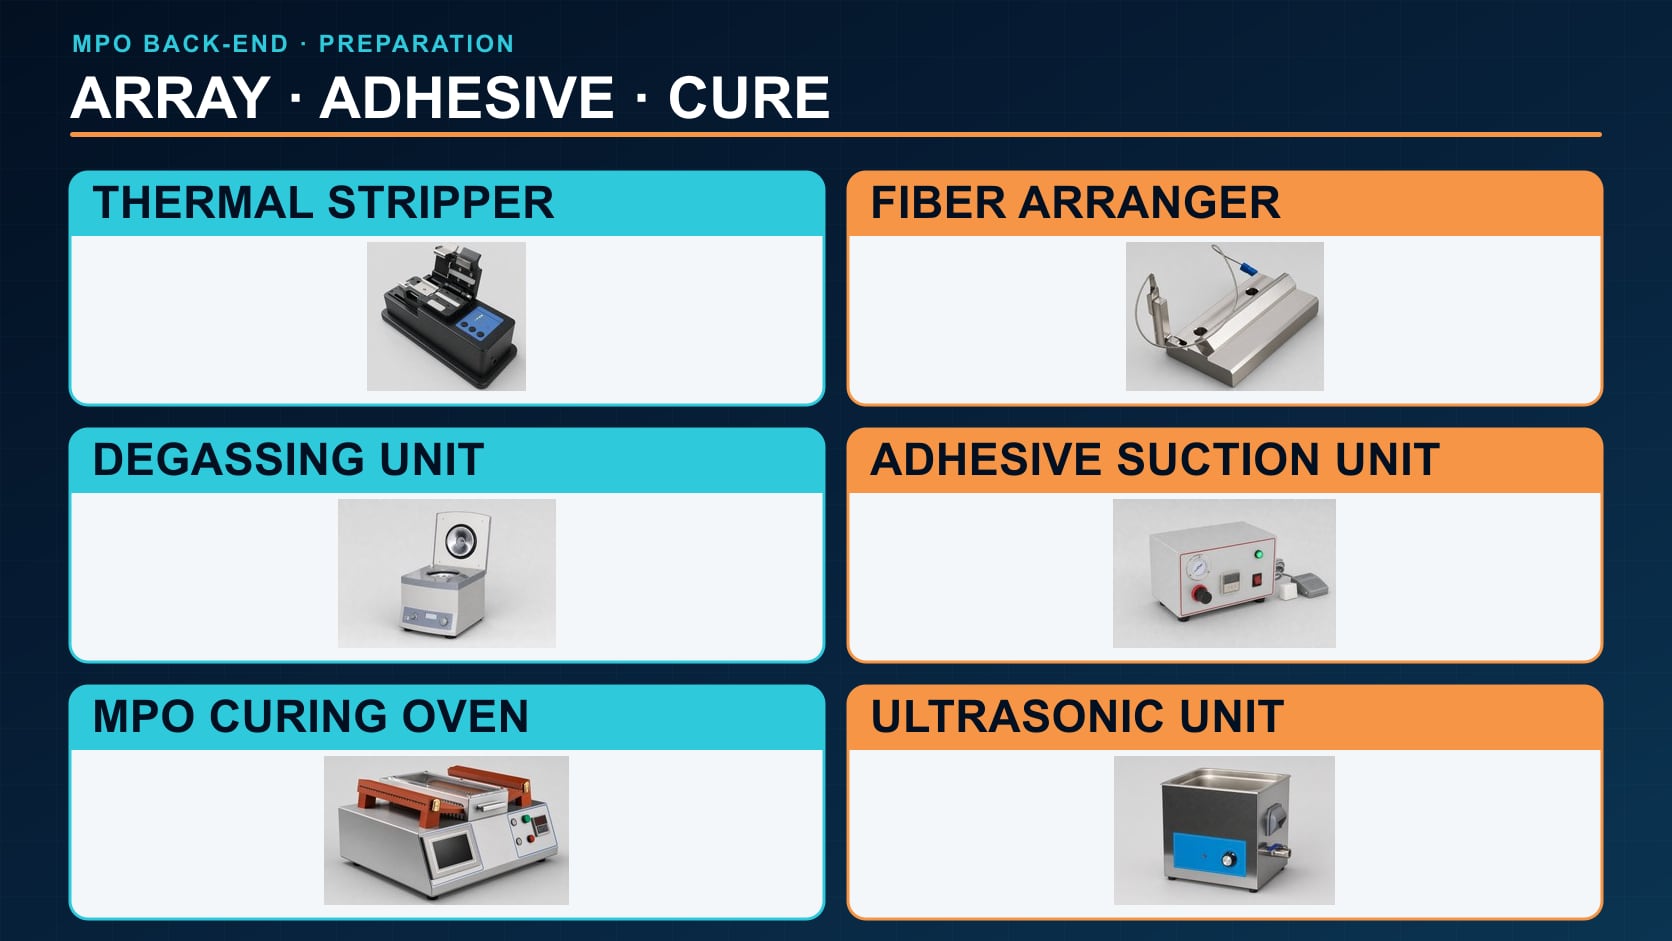
Supplier-quoted, source-backed 3D reference: stripping, array handling, adhesive, cure and ultrasonic equipment. Branding and model text are removed.
-
Cable-end preparation. This required operation measures, cuts and opens the cable, prepares the aramid and preloads connector parts. It is absent from the quoted list. Verify the cable identity, dimensions, orientation, preload order and prepared end.
-
Pengupas serat termal MPO. This conditional tool exposes the specified bare-fiber length. Use it only with a compatible fiber and coating. Keep the setting, strip length and damage check from the actual cable.
-
Pengatur susunan serat telanjang. This required device places the separated fibers in one linear order. It follows the channel map; it does not create polarity. Keep a position-by-position check or identified array image.
-
Fiber-array holding clamps. Klem yang diperlukan ini menjaga pesanan yang telah diverifikasi tetap stabil selama pemuatan. Konfirmasi jumlah serat, jarak antar serat (pitch), dan kecocokan material. Simpan ID fixture dan lakukan inspeksi setelah penggunaan klem.
Decision criterion: The cable reel, cut length, fiber identities, end orientation and channel map must share one traveler before adhesive loading.
Prepare adhesive and load the ferrule
-
Unit degassing perekat sentrifugal. This conditional unit prepares a controlled adhesive batch when the material instruction requires it. Link the adhesive name, lot, usable-life status, quantity and cycle to the loaded ferrules.
-
Unit hisap perekat ferrule MPO. The quotation identifies this conditional equipment category; it does not establish a universal ferrule-filling route or acceptance condition. Use it only when the signed connector and material instruction specifies it. Keep the equipment ID, component and material lots, settings and the process verification required by that instruction.
-
Operasi pemasangan ferrule. This required step inserts the ordered fibers into the ferrule. The list names no separate powered loader. Keep the ferrule lot, orientation and loaded-array check.
-
Perekat dan cairan proses. These are specified materials, not a catalog-defined recipe. Control their identity, lot, shelf life, preparation and working time.
Instruksi kerja harus menetapkan urutan pemuatan perekat dan serat. Harga pemasok, total, detail kontak, dan ketentuan komersial tidak dipublikasikan.
Cure the ferrule and assemble connector hardware
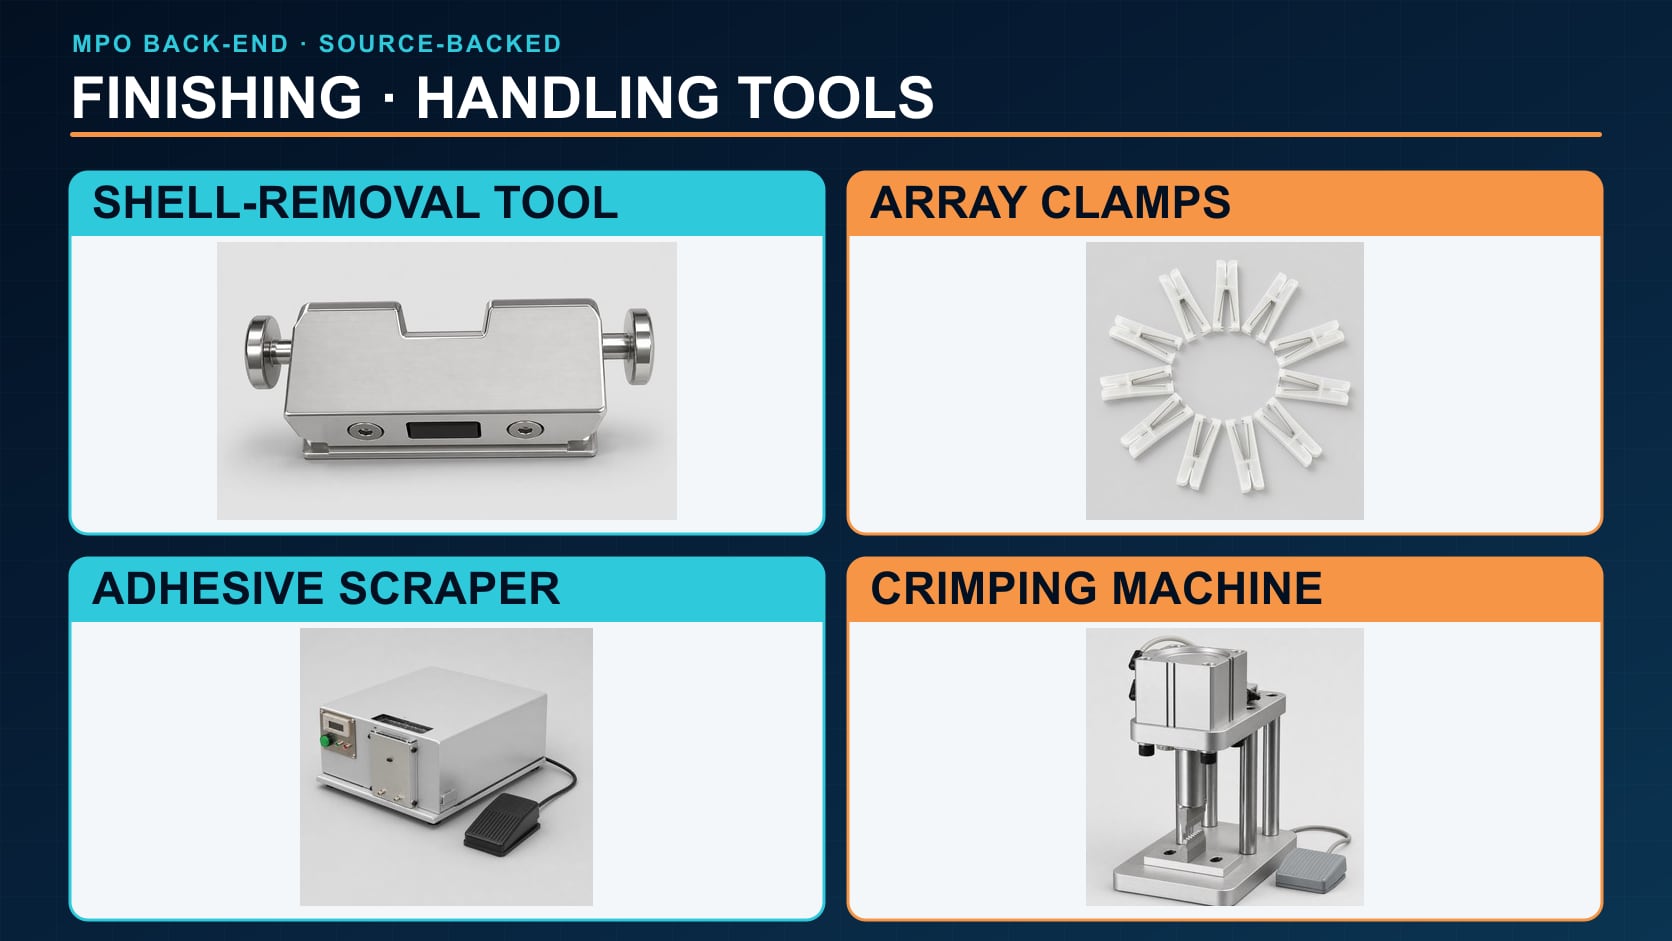
Supplier-quoted, source-backed 3D reference: shell removal, array holding, adhesive scraping and crimping. Branding and model text are removed.
-
Oven pemanas MPO. This required station cures the loaded ferrule in a compatible holder. Keep the adhesive batch, recipe, holder, load, time-temperature evidence and post-cure check. Two quoted ovens do not prove capacity or required redundancy.
-
Mesin penghilang perekat atau mesin pengikis. This conditional machine removes the specified cured material. Define its target, removal boundary and normal or rework status. Keep actual-ferrule before-and-after images and the damage check.
-
Persiapan serat yang menonjol dan perekat yang telah mengeras. Langkah wajib ini membuat ferrule yang telah dikeringkan siap untuk dipoles. Proses konektor harus menyebutkan metode yang diizinkan. Simpan revisinya, identitas ferrule, dan pemeriksaan persiapan.
-
Pneumatic connector crimping press. This conditional press assembles compatible hardware or strength-member parts at the connector-defined stage. Prove the jaw and tooling with the actual housing and aramid setup. Keep the tooling ID and assembly inspection.
-
Alat pelepas rumah konektor. This is a rework tool unless the connector instruction states otherwise. Define its permitted use, housing match and rework limit. Repeat the required inspection, polarity and optical checks after reassembly.
-
Unit proses ultrasonik. This unit remains conditional because its object, liquid, timing and material compatibility are not yet defined. If selected, keep those inputs, cycle settings and before-and-after inspection.
Semir ferrule MPO yang dipilih
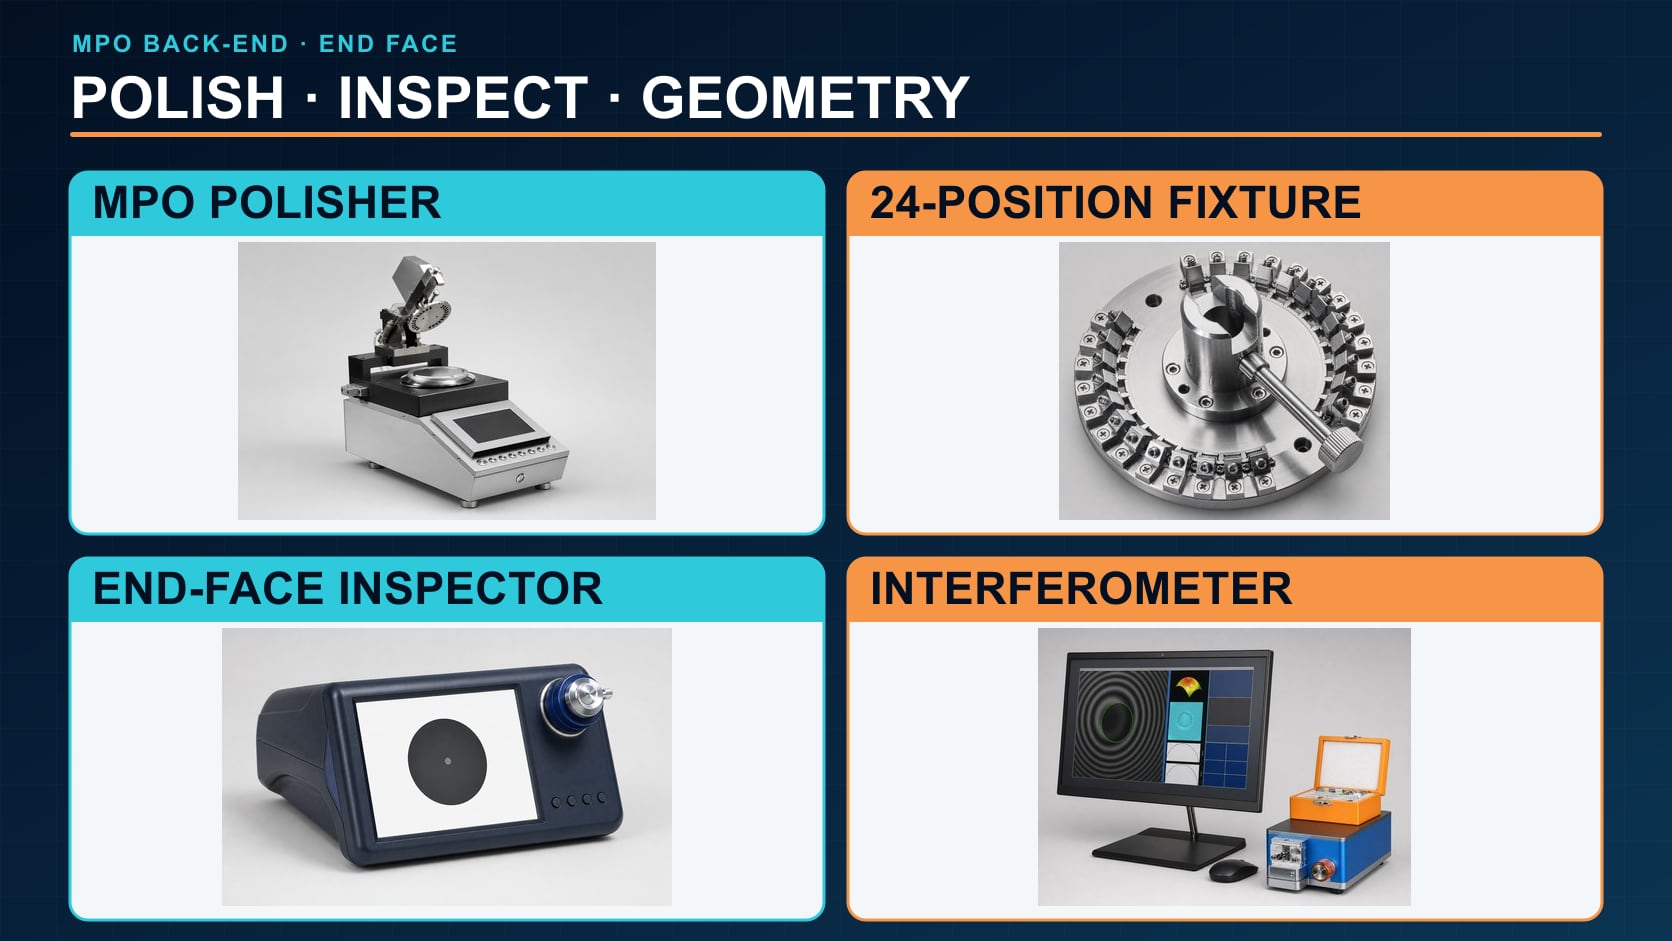
Supplier-quoted, source-backed 3D reference: MPO polishing, full-array inspection and rectangular-ferrule geometry measurement.
-
Mesin poles MPO. This required machine runs the multi-stage surface-finishing route. The recipe defines load, time, fixture, cleaning and allowed rework. Keep the machine, program, recipe and rework history.
-
24-position UPC and APC fixtures. Select the fixture that matches each purchased polish. “24-position” is fixture capacity, not fiber count or guaranteed throughput. Keep the fixture ID and result for every loaded position.
-
Bantalan, film, kain, dan cairan. Bahan habis pakai ini bekerja sebagai resep yang disesuaikan. Daftar saja tidak menetapkan urutan, masa pakai, atau kompatibilitasnya. Simpan identitas material, nomor lot, status penggunaan, dan revisi resep.
Clean, inspect and measure the ferrule
-
MPO end-face inspection system. This required gate evaluates the rectangular contact area and every fiber position with a qualified MPO adapter. Keep the image, adapter, method, criteria revision and clean-reinspect-disposition chain. It does not replace geometry or optical testing.
-
MPO ferrule geometry interferometer. This conditional instrument measures specified rectangular-ferrule geometry. The control plan decides full inspection or sampling. Keep the reference state, adapter, raw report, repeatability evidence and product limits.
IEC 61300-3-35:2022 covers visual inspection and classification for contamination, scratches and defects. It includes the complete contact surface of rectangular ferrules and separates visual inspection from other measurements. When geometry evidence is required, IEC 61300-3-30:2026 menggambarkan pengukuran atribut ujung muka yang ditentukan untuk ferrule multi-serat persegi panjang yang berlaku.
Verify channel mapping and optical performance

Supplier-quoted, source-backed 3D reference: end-face, geometry, polarity and multi-channel optical test equipment.
-
Penguji polaritas MPO atau urutan serat. This required station compares both connector ends with the signed map. It detects an error; it does not define or correct the map. Challenge the actual gender and key orientation, then save every channel result.
-
Multimode MPO optical test system. This required station measures the specified channels of the reference multimode assembly. Confirm the wavelengths, metrics, method, directions and limits. Keep the tester, adapters, reference cords, calibration state, setup and raw values. Scope single-mode or return-loss needs separately.
How to verify: Follow one identified launch assembly through the complete route. Retrieve its cable-reel data, array map, material and cure lots, tooling, rework history, inspection images and required test files. Machine operation alone is not proof that the connected process can release the product.
Bukti Pelepasan untuk Kabel dan Rakitan MPO Jadi
No single pass/fail number covers every failure layer. The base cable needs release evidence before connectorization. The finished assembly then needs channel-specific inspection, mapping and optical results.
| Failure layer | Detecting gate | Release record |
|---|---|---|
| Buffer ketat atau jaket | Dimensions, process checks and reel inspection | Pengukuran dan hasil gulungan yang diidentifikasi |
| Cable optical path | Finished-reel optical test by identified fiber | Metode, pengaturan, dan hasil serat mentah |
| Persiapan serat | Preparation inspection and continuity or downstream result | Prepared-end check and disposition |
| Array order | Pemeriksaan array ditambah uji polaritas akhir atau urutan | Signed map and every channel result |
| Perekat dan pengawetan | Material, preparation and approved cure controls plus inspection | Lots, recipe, cycle and post-cure result |
| Permukaan ujung yang dipoles | Full-array visual inspection | Identified image and clean-reinspect-disposition history |
| Ferrule geometry | Gerbang interferometer jika ditentukan | Identified raw report and applicable limits |
| Jalur optik selesai | Channel-level optical test | Equipment, reference setup, raw values and limits |
| Traceability | Tinjauan pelancong dan berkas data | One identity linking assembly, lots and results |
Gerbang-gerbang ini menjawab pertanyaan yang berbeda. Gambar ujung bersih tidak membuktikan geometri, polaritas, atau kinerja optik. Lulus uji optik tidak menggantikan catatan tahap kabel.
IEC 61300-3-4:2023 describes attenuation-measurement methods for optical components. The buyer must still select the method, source conditions, reference arrangement, wavelengths, directions, limits and sampling. If return loss is required, name the equipment and method explicitly; “MPO tester” is not enough.
Pitfalls: Test software uses different channel numbers from the assembly drawing. Rework overwrites the failed result. Master cords or adapters lack identities. Cable and connector records cannot be joined under one assembly ID.
Tidak ada bukti yang mendukung menyebut satu cacat secara universal sebagai “paling umum.” Pasang gerbang deteksi di setiap lapisan kegagalan dan simpan catatan terkait tersebut.
FAT Launch Product and Record Package
Use the signed launch product for FAT, not a convenient demonstration sample. A 12-core GJFJV-to-MPO trunk is representative only after its cable drawing, ferrule, key orientation, polarity, polish and optical plan are signed. Demonstrate the purchased cable and back-end route under the same traceability identity.
| FAT gate | Representative run | Catatan untuk disimpan |
|---|---|---|
| Input dan produksi kabel | Lepaskan material; buat buffer ketat dan kabel dasar GJFJV | Lot, gulungan masuk, pengaturan, alarm, dimensi, dan identitas gulungan jadi |
| Cable release | Jalankan rencana dimensi, optik, dan mekanis yang telah ditandatangani | Methods, equipment, calibration state, raw results and disposition |
| Persiapan ujung dan susunan | Cut and open the cable; identify, strip, arrange and load the fibers | Pemeriksaan ujung yang telah disiapkan, peta saluran, lot ferrule, dan perekat |
| Cure and hardware | Complete cure and connector assembly at the defined stage | Status resep, batch, pemegang, perkakas, dan perakitan |
| Mengilapkan dan membersihkan | Use the matched machine, fixture and consumables | Recipe revision, fixture, consumable lots and rework history |
| End face and geometry | Periksa setiap posisi; ukur geometri bila ditentukan | Saved images and the identified geometry report when required |
| Mapping and optics | Verify the signed map; test every required channel | Orientation, setup, wavelengths, directions, raw values and limits |
| Handover | Pembeli mengulangi operasi yang disepakati dan mengambil datanya | Training, manuals, spares, consumables and open-item log |
Evidence to request: The data package must trace a finished channel back to its connector, ferrule, adhesive, prepared cable length, source reel and cable-production record.
Back-end inspection and test equipment are essential parts of the complete-project FAT. One successful run approves only the documented product, tooling and method range. Expansion needs a written compatibility or requalification decision.
Peter Dia reviewed the project scope used in this article. His input was specific: treat cable-stage results and finished-assembly results as separate acceptance layers. Include the applicable back-end inspection and test route in FAT. These boundaries apply to the signed launch product; they are not a universal MPO recipe.
Batas Tanggung Jawab Proyek Lengkap HONGKAI
HONGKAI insight: HONGKAI can contract the integrated scope. HONGKAI engineers the GJFJV cable-making route and coordinates verified specialist MPO assembly, inspection and test stations. The signed responsibility matrix, launch product and FAT plan—not the catalog or quotation alone—control the final equipment list and delivery scope.
| Scope block | Reference responsibility | Apa yang harus dinyatakan dalam kontrak |
|---|---|---|
| HK-30 and GJFJV phases | Lingkup pembuatan kabel HONGKAI | Product range, configuration, cage arrangement, tooling, FAT and training |
| Cable laboratory | Integrated or buyer-supplied by agreement | Instrumen, metode, kalibrasi, utilitas, dan pengambilan sampel |
| MPO assembly equipment | Specialist equipment integrated into the project | Source, fixtures, work instructions, consumables, FAT and training |
| Inspeksi dan pengujian MPO | Specialist equipment integrated into the project | Compatibility, adapters, software, data fields and calibration |
| Site, documents and samples | Assigned in the contract | Utilitas, gambar, komponen, batas, sampel, dan persetujuan |
| Installation and after-sales | Named by equipment group | Lead party, specialist participation, escalation and spares |
What to ask: Require one responsibility matrix rather than separate supplier promises. Public equipment images are presentation references; the signed list, drawings and FAT machines control delivery.
Daftar Periksa:
-
☐ Rencana jalur kabel dan laboratorium sesuai dengan rencana konstruksi GJFJV yang telah ditandatangani
-
☐ Every back-end machine and fixture maps to the launch connector process
-
☐ Array order and final polarity use the same signed channel map
-
☐ Gerbang visual, geometri, dan optik memiliki bukti penerimaan terpisah
-
☐ Cable and assembly records share one traceability chain
-
☐ Responsibilities are named, and FAT retains raw data instead of pass labels
A complete line is not complete just because every machine is present. It becomes complete when one approved product moves from verified cable inputs to release with linked process and test evidence.



