


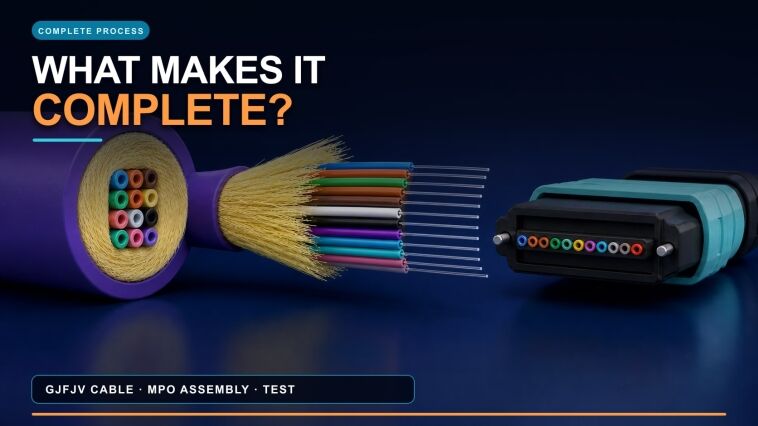
A buyer planning an MPO cable manufacturing process has one central decision. Can the proposed scope release the finished assembly with every channel identified and tested? That decision is broader than choosing a polishing machine.
A complete project links two systems. The GJFJV-type cable route makes and bundles the individual tight-buffered fibers. The MPO workcell then separates, orders and loads them into the ferrule. Both the base cable and the finished assembly need their own release evidence.

Verified-structure 3D reference: this 12-core GJFJV example has a bundled core. The ordered row is formed during ferrule preparation; the signed product drawing controls the saleable construction.
This distinction matters because MPO is a connector interface, not a universal cable construction. The project in this guide uses an indoor multi-core GJFJV-type tight-buffer cable as the reference input. A different launch cable, ferrule family, polarity or optical specification can change the machines, fixtures, test paths and FAT sample.
기존 단일 광섬유 커넥터 작업 흐름은 다음을 참조하세요. 광섬유 패치코드 생산 가이드. 해당 경로는 이 MPO 작업 셀의 장비 목록이 아닙니다.
전체 라인 견적 전에 확정할 범위
Freeze the finished assembly, base-cable drawing and release evidence before choosing equipment. An “MPO line” quotation is incomplete without the cable construction, fiber count, connector interface, key orientation, polarity, polish, optical method and traceability unit. These inputs determine the cable-line configuration and the back-end fixtures.
IEC 60794-2-23:2024 addresses indoor multi-fiber cables used in MPO-terminated assemblies. IEC 61754-7-1:2014 그리고 IEC 61754-7-2:2017 cover one-row and two-row MPO interface variants. These publications help define the relevant product and interface layers. The buyer still has to approve the cable drawing, materials, process route and acceptance limits.
| 정지 입력 | 구매자 결정 | Equipment consequence |
|---|---|---|
| 완제품 | 명칭이 지정된 어셈블리, 길이 및 분기 형식 | 절단, 피복 제거, 취급, 라벨링 및 테스트 접근 |
| 케이블 구조 | 광섬유 수, 타이트 버퍼 배열, 아라미드 시스템 및 재킷 | 페이오프, 가이더, 압출 툴링, 가이드 및 테이크업 |
| Connector system | 페룰 열, 성별, 키 방향, 하우징 및 폴리시 | 로딩 및 경화 홀더, 연마 고정구 및 테스트 어댑터 |
| 광섬유 및 채널 맵 | 광섬유 카테고리, 수량, 위치 맵 및 종단 간 극성 | 어레이 픽스처, 작업 지침서, 극성 테스터 및 데이터 필드 |
| Cable acceptance | 치수, 광학 및 기계적 요구사항, 시험 방법 및 샘플링 | Online gauges plus separately scoped cable-laboratory equipment |
| Assembly acceptance | End-face, geometry when required, polarity and optical requirements | Inspector, interferometer when required, channel tester and data system |
| Traceability unit | Reel, cut length, connector pair, component lots and traveler identity | Barcode or traveler fields, data export and rework history |
In this guide, the launch product is the signed assembly used to prove the purchased route. A traveler is the linked production record that follows that assembly. Factory acceptance testing (FAT) must connect the launch product, traveler and raw result files.
Decision criterion: This guide uses a Make–Map–Prove–Trace test for quotation completeness. Make the signed base cable. Map every fixture, adapter and software path to the launch product. Prove cable release and finished-assembly release at separate gates. Trace each tested channel back to its source reel, components and process records. If any step lacks named equipment, method or retained evidence, the quoted scope is not yet complete. Approve expansion only for named future products.
GJFJV Cable Making in Two Manufacturing Phases
The verified HONGKAI reference has two manufacturing phases. HK-30 makes the individual tight-buffered fibers. The configured GJFJV phase gathers them, applies the aramid system and extrudes the common jacket. The quotation must state whether the gathering cage is integrated with HK-50 or supplied as a matched unit.
HONGKAI reference route: tight buffering, multi-fiber gathering, aramid application and common-jacket extrusion. The signed project controls the final station arrangement.
Four stages in the GJFJV cable route
-
Tight buffer — Protect each fiber. Pay off the identified fiber, apply the tight buffer, cool it, check the required dimensions and wind the finished buffered fiber.
-
섬유를 모으고 — 케이블 코어를 만듭니다. 식별된 타이트 버퍼 피복 광섬유를 설정된 집합 시스템에 적재하십시오. 케이블 도면에 표시된 번들형 코어를 형성하십시오.
-
강도 시스템 추가 — 아라미드 원사를 적용합니다. 지정된 아라미드 원사를 제어된 장력 하에서 배치하십시오. 섬유와 원사를 재킷 툴링으로 유도하십시오.
-
재킷 및 릴 — 베이스 케이블을 마무리합니다. 공통 재킷을 압출 성형하고 냉각합니다. 필요한 치수를 확인한 후 추적 가능한 완제품 릴에 감습니다.
그만큼 HONGKAI GJFJV 생산 라인 페이지 shows the HK-30 tight-buffer phase and an HK-50 reference line. The visible functions include fiber gathering, aramid payoff, jacket extrusion, cooling, diameter measurement, capstan and take-up. This is configuration evidence, not a universal fiber count, material, speed or layout.
최종 조립으로 연기되어서는 안 되는 케이블 스테이지 데이터
Online diameter display is useful, but one screen value is not a complete cable release. The quotation should state which data are displayed, stored or checked offline and which laboratory instruments are included.
| Control point | 보관할 기록 | 별도의 장비 또는 범위를 정하기 위한 결정 |
|---|---|---|
| 입력 광섬유 | 릴 식별 정보, 승인된 광섬유 사양 및 기준 증거 | 입고 광학 검사 방법 및 샘플링 계획 |
| 타이트 버퍼 단계 | 자재 로트, 광섬유 식별 정보, 공정 설정, 경보 및 측정된 치수 | 필요 시 오프라인 치수 또는 동심도 측정 방법 |
| 집합 및 재킷 공정 | 버퍼드 파이버 릴 식별 정보, 아라미드 및 재킷 로트, 라인 설정, 경보 및 직경 증거 | 데이터 로깅 옵션 및 오프라인 단면 측정 |
| Finished cable reel | 릴 길이/식별, 외관 및 치수 검사, 연속성 및 합의된 광학적 결과 | Optical test instruments, reference method and record format |
| Cable qualification | 승인된 케이블 사양에서 요구하는 결과 | 인장, 압축, 굽힘, 온도 또는 기타 프로젝트별 실험실 장비 |
Common mistakes: A buyer budgets only the extrusion line because it includes a diameter gauge. Optical and mechanical release tests then remain undefined. A later MPO result cannot replace the base cable’s own acceptance record.
The supplier quotation reviewed for this article contains no cable-making or cable-laboratory equipment. Those items must be added to the complete-project scope rather than inferred from the back-end equipment list.
MPO 어셈블리를 위한 완전한 백엔드 장비 공정
GJFJV 케이블은 개별적으로 타이트 버퍼 처리된 광섬유 묶음을 이 워크셀로 가져옵니다. 직선형 배열은 커넥터 조립 시에만 형성됩니다. 서명된 channel map—양쪽 커넥터 단자의 위치 대 위치 도면—은 광섬유의 순서와 극성을 제어합니다.
The supplier quotation identifies equipment for array preparation, adhesive handling, cure, polish, inspection and test. It does not establish the production sequence or process settings. The signed bill of materials, connector instruction and release plan must do that.
The evidence boundary is explicit. The public HONGKAI GJFJV page supports cable-line functions. The supplied MPO catalog and quotation support equipment categories and source geometry. The cited IEC publications support interface and test-method layers. None of these sources establishes a universal recipe, throughput, acceptance limit, certification or customer result. The source-backed 3D images preserve the catalog structures while supplier brands, model text, prices and commercial terms remain excluded.
케이블 단부에서 해제된 어셈블리까지의 네 단계
-
준비 및 식별 — 모든 광섬유를 노출시키고 정렬합니다. 섬유 식별을 잃지 않고 케이블 단자를 개방하십시오. 서명된 채널 맵에 따라 모든 섬유를 정렬하십시오.
-
Load and stabilize — Use the qualified adhesive and ferrule route. 지정된 접착제를 준비합니다. 검증된 제품별 순서에 따라 광섬유와 페룰을 장전합니다.
-
페룰 마무리 — 경화, 준비, 연마 및 검사. 페룰을 경화 및 준비한 후 다단계 연마를 수행합니다. 커넥터에서 정의된 지점에 하드웨어를 조립하고 청소된 단면을 검사합니다.
-
Verify and release — Confirm geometry, mapping and optics. 필요할 경우 형상을 측정하십시오. 연결된 레코드 패키지를 출시하기 전에 채널 맵과 광학 결과를 확인하십시오.
런칭 프로젝트의 경우, 각 장비 항목은 세 가지 범위 라벨 중 하나에 매핑됩니다. 필수 이 런치 경로에 필요한 수단이며, 모든 MPO 설계에 필요한 것은 아님. Conditional 서명된 공정에서 요구할 경우에만 장비가 투입된다.
Rework equipment stays outside normal production unless an authorized instruction allows its use. This project-specific mapping prevents optional or rework tools from becoming a false universal line. During FAT, run each applicable item with the launch product and keep the device-specific proof named below.
섬유를 준비하고 식별합니다
견적 목록은 어레이 준비부터 시작됩니다. 완전한 워크셀에는 케이블 측정 및 절단, 재킷 제거, 아라미드 준비 및 필요한 구성품 프리로딩도 포함되어야 합니다.
Supplier-quoted, source-backed 3D reference: stripping, array handling, adhesive, cure and ultrasonic equipment. Branding and model text are removed.
-
케이블 단자 준비. This required operation measures, cuts and opens the cable, prepares the aramid and preloads connector parts. It is absent from the quoted list. Verify the cable identity, dimensions, orientation, preload order and prepared end.
-
MPO 열광섬유 벗김기. This conditional tool exposes the specified bare-fiber length. Use it only with a compatible fiber and coating. Keep the setting, strip length and damage check from the actual cable.
-
벌거벗은 섬유 어레이 정렬기. This required device places the separated fibers in one linear order. It follows the channel map; it does not create polarity. Keep a position-by-position check or identified array image.
-
광섬유 어레이 고정 클램프. These required clamps keep the verified order stable during loading. Confirm the fiber count, pitch and material match. Keep the fixture ID and post-clamp inspection.
판단 기준: 케이블 릴, 절단 길이, 광섬유 식별 정보, 단부 방향 및 채널 맵은 접착제 적재 전에 하나의 트래블러를 공유해야 한다.
Prepare adhesive and load the ferrule
-
Centrifugal adhesive degassing unit. This conditional unit prepares a controlled adhesive batch when the material instruction requires it. Link the adhesive name, lot, usable-life status, quantity and cycle to the loaded ferrules.
-
MPO 페룰 접착-흡착 유닛. The quotation identifies this conditional equipment category; it does not establish a universal ferrule-filling route or acceptance condition. Use it only when the signed connector and material instruction specifies it. Keep the equipment ID, component and material lots, settings and the process verification required by that instruction.
-
페룰 로딩 작업. 이 필수 단계에서는 주문한 광섬유를 페룰에 삽입합니다. 목록에는 별도의 동력식 로더가 명시되어 있지 않습니다. 페룰 로트, 방향 및 적재된 어레이 점검을 유지하십시오.
-
Adhesives and process liquids. 이들은 카탈로그에 정의된 조제법이 아닌, 명시된 재료입니다. 이들의 정체성, 로트, 유효기간, 준비 및 작업 시간을 관리하세요.
The work instruction must define the adhesive-and-fiber loading sequence. Supplier prices, totals, contact details and commercial terms are not published.
페룰을 경화시키고 커넥터 하드웨어를 조립합니다.
Supplier-quoted, source-backed 3D reference: shell removal, array holding, adhesive scraping and crimping. Branding and model text are removed.
-
MPO 경화 오븐. This required station cures the loaded ferrule in a compatible holder. Keep the adhesive batch, recipe, holder, load, time-temperature evidence and post-cure check. Two quoted ovens do not prove capacity or required redundancy.
-
접착제 제거 또는 긁어내기 기계. This conditional machine removes the specified cured material. Define its target, removal boundary and normal or rework status. Keep actual-ferrule before-and-after images and the damage check.
-
돌출된 섬유 및 경화된 접착제 준비. 이 필수 단계는 경화된 페룰을 연마 준비 상태로 만든다. 커넥터 공정은 허용된 방법을 명시해야 한다. 해당 방법의 개정판, 페룰 식별 정보 및 준비 점검사항을 유지하라.
-
공기압식 커넥터 압착 프레스. This conditional press assembles compatible hardware or strength-member parts at the connector-defined stage. Prove the jaw and tooling with the actual housing and aramid setup. Keep the tooling ID and assembly inspection.
-
커넥터 쉘 제거 도구. This is a rework tool unless the connector instruction states otherwise. Define its permitted use, housing match and rework limit. Repeat the required inspection, polarity and optical checks after reassembly.
-
초음파 공정 장치. This unit remains conditional because its object, liquid, timing and material compatibility are not yet defined. If selected, keep those inputs, cycle settings and before-and-after inspection.
선택한 MPO 페룰을 연마하세요
Supplier-quoted, source-backed 3D reference: MPO polishing, full-array inspection and rectangular-ferrule geometry measurement.
-
MPO 연마기. This required machine runs the multi-stage surface-finishing route. The recipe defines load, time, fixture, cleaning and allowed rework. Keep the machine, program, recipe and rework history.
-
24-position UPC and APC fixtures. Select the fixture that matches each purchased polish. “24-position” is fixture capacity, not fiber count or guaranteed throughput. Keep the fixture ID and result for every loaded position.
-
패드, 필름, 천 및 액체. These consumables work as a matched recipe. The list alone does not establish their order, life or compatibility. Keep material identities, lots, usage status and recipe revision.
Clean, inspect and measure the ferrule
-
MPO 단면 검사 시스템. This required gate evaluates the rectangular contact area and every fiber position with a qualified MPO adapter. Keep the image, adapter, method, criteria revision and clean-reinspect-disposition chain. It does not replace geometry or optical testing.
-
MPO 페룰 형상 간섭계. This conditional instrument measures specified rectangular-ferrule geometry. The control plan decides full inspection or sampling. Keep the reference state, adapter, raw report, repeatability evidence and product limits.
IEC 61300-3-35:2022 covers visual inspection and classification for contamination, scratches and defects. It includes the complete contact surface of rectangular ferrules and separates visual inspection from other measurements. When geometry evidence is required, IEC 61300-3-30:2026 해당 사각형 다중 광섬유 페룰의 지정된 단면 속성 측정 방법을 설명한다.
채널 매핑 및 광 성능을 확인하세요
Supplier-quoted, source-backed 3D reference: end-face, geometry, polarity and multi-channel optical test equipment.
-
MPO 극성 또는 광섬유 순서 테스터. This required station compares both connector ends with the signed map. It detects an error; it does not define or correct the map. Challenge the actual gender and key orientation, then save every channel result.
-
다중 모드 MPO 광 테스트 시스템. This required station measures the specified channels of the reference multimode assembly. Confirm the wavelengths, metrics, method, directions and limits. Keep the tester, adapters, reference cords, calibration state, setup and raw values. Scope single-mode or return-loss needs separately.
How to verify: Follow one identified launch assembly through the complete route. Retrieve its cable-reel data, array map, material and cure lots, tooling, rework history, inspection images and required test files. Machine operation alone is not proof that the connected process can release the product.
케이블 및 완성된 MPO 어셈블리에 대한 출하 증빙 자료
No single pass/fail number covers every failure layer. The base cable needs release evidence before connectorization. The finished assembly then needs channel-specific inspection, mapping and optical results.
| Failure layer | Detecting gate | Release record |
|---|---|---|
| 타이트 버퍼 또는 재킷 | 치수, 공정 검사 및 릴 검사 | 확인된 측정값 및 릴 결과 |
| 케이블 광경로 | 식별된 광섬유에 의한 완제 릴 광학 테스트 | 방법, 설정 및 원시 섬유 결과 |
| 섬유 준비 | Preparation inspection and continuity or downstream result | 준비된 단자 점검 및 처분 |
| Array order | 어레이 점검 및 최종 극성 또는 순서 테스트 | 서명된 맵 및 모든 채널 결과 |
| 접착제 및 경화 | Material, preparation and approved cure controls plus inspection | 로트, 레시피, 사이클 및 포스트 경화 결과 |
| 광택 처리된 단면 | Full-array visual inspection | 식별된 이미지 및 청정 재검사 처분 이력 |
| Ferrule geometry | 지정된 경우 간섭계 게이트 | 식별된 원시 보고서 및 적용 가능한 한계 |
| Finished optical path | 채널 수준 광학 테스트 | Equipment, reference setup, raw values and limits |
| Traceability | 트래블러 및 데이터 파일 검토 | One identity linking assembly, lots and results |
이러한 검사 항목들은 서로 다른 질문에 답한다. 깨끗한 단면 이미지는 기하학적 특성, 극성 또는 광학 성능을 증명하지 않는다. 광학 통과 시험이 케이블 단계 기록을 대체하지 않는다.
IEC 61300-3-4:2023 describes attenuation-measurement methods for optical components. The buyer must still select the method, source conditions, reference arrangement, wavelengths, directions, limits and sampling. If return loss is required, name the equipment and method explicitly; “MPO tester” is not enough.
Pitfalls: Test software uses different channel numbers from the assembly drawing. Rework overwrites the failed result. Master cords or adapters lack identities. Cable and connector records cannot be joined under one assembly ID.
어떤 결함을 보편적으로 “가장 흔한” 결함이라고 부를 근거는 존재하지 않는다. 모든 고장 단계에 탐지 게이트를 설치하고 연결된 기록을 보존하라.
FAT 출시 제품 및 기록 패키지
Use the signed launch product for FAT, not a convenient demonstration sample. A 12-core GJFJV-to-MPO trunk is representative only after its cable drawing, ferrule, key orientation, polarity, polish and optical plan are signed. Demonstrate the purchased cable and back-end route under the same traceability identity.
| FAT gate | Representative run | 보관할 기록 |
|---|---|---|
| 입력 및 케이블 생산 | 재료를 방출하여 타이트 버퍼와 GJFJV 베이스 케이블을 제작합니다. | 로트, 입력 릴, 설정, 알람, 치수 및 완제품 릴 식별 정보 |
| Cable release | 서명된 치수, 광학 및 기계 도면을 실행하십시오. | 방법, 장비, 교정 상태, 원시 결과 및 처분 |
| 단말 및 어레이 준비 | Cut and open the cable; identify, strip, arrange and load the fibers | Prepared-end check, channel map, ferrule and adhesive lots |
| Cure and hardware | Complete cure and connector assembly at the defined stage | Recipe, batch, holder, tooling and assembly status |
| 광택 내고 청소하기 | Use the matched machine, fixture and consumables | Recipe revision, fixture, consumable lots and rework history |
| 단면 및 형상 | 모든 위치를 점검하고, 지정된 경우 형상을 측정하십시오. | Saved images and the identified geometry report when required |
| Mapping and optics | Verify the signed map; test every required channel | 방향, 설정, 파장, 방향, 원시 값 및 한계 |
| Handover | Buyer repeats the agreed operation and retrieves its data | 교육, 매뉴얼, 예비품, 소모품 및 미해결 항목 로그 |
Evidence to request: The data package must trace a finished channel back to its connector, ferrule, adhesive, prepared cable length, source reel and cable-production record.
Back-end inspection and test equipment are essential parts of the complete-project FAT. One successful run approves only the documented product, tooling and method range. Expansion needs a written compatibility or requalification decision.
피터 히 reviewed the project scope used in this article. His input was specific: treat cable-stage results and finished-assembly results as separate acceptance layers. Include the applicable back-end inspection and test route in FAT. These boundaries apply to the signed launch product; they are not a universal MPO recipe.
HONGKAI 완공 프로젝트 책임 경계
HONGKAI insight: HONGKAI can contract the integrated scope. HONGKAI engineers the GJFJV cable-making route and coordinates verified specialist MPO assembly, inspection and test stations. The signed responsibility matrix, launch product and FAT plan—not the catalog or quotation alone—control the final equipment list and delivery scope.
| Scope block | Reference responsibility | 계약서에 명시되어야 할 사항 |
|---|---|---|
| HK-30 and GJFJV phases | HONGKAI 케이블 제조 범위 | 제품 범위, 구성, 케이지 배열, 공구, FAT 및 교육 |
| Cable laboratory | 통합 또는 구매자 제공(계약에 따라) | Instruments, methods, calibration, utilities and sampling |
| MPO 조립 장비 | 프로젝트에 통합된 전문 장비 | Source, fixtures, work instructions, consumables, FAT and training |
| MPO inspection and test | 프로젝트에 통합된 전문 장비 | Compatibility, adapters, software, data fields and calibration |
| Site, documents and samples | 계약서에 명시됨 | Utilities, drawings, components, limits, samples and approvals |
| 설치 및 애프터서비스 | Named by equipment group | Lead party, specialist participation, escalation and spares |
What to ask: Require one responsibility matrix rather than separate supplier promises. Public equipment images are presentation references; the signed list, drawings and FAT machines control delivery.
체크리스트:
-
☐ 케이블 라인 및 실험실 계획이 서명된 GJFJV 시공 도면과 일치함
-
☐ 모든 백엔드 기계 및 고정구는 런치 커넥터 공정에 매핑됨
-
☐ Array order and final polarity use the same signed channel map
-
☐ 비주얼, 기하학 및 광학 게이트는 별도의 승인 증거를 보유함
-
☐ 케이블과 조립 기록은 하나의 추적성 체인을 공유합니다
-
☐ Responsibilities are named, and FAT retains raw data instead of pass labels
A complete line is not complete just because every machine is present. It becomes complete when one approved product moves from verified cable inputs to release with linked process and test evidence.
