


A cable factory considering a copper wire drawing machine should start with its wire demand, not a machine catalogue. The first decision is whether to keep buying wire at the required size or bring some of that work in-house.
Before comparing machines, confirm how much copper the factory uses each month, which wire sizes it needs and whether the finished wire must be annealed. Then compare the full cost of buying wire with the cost of producing acceptable wire in-house.
This guide helps factory owners and technical buyers make that comparison. It does not assume that every cable factory needs a drawing line, or that one monthly volume guarantees savings.
Is Monthly Copper Use High Enough to Evaluate Drawing In-House?
In HONGKAI’s buying discussions, copper use of around four metric tonnes per month is an initial reference for evaluating in-house drawing. That figure comes from practical sales-planning experience, not a universal minimum or a calculated break-even point. It does not prove that a particular machine will save money.
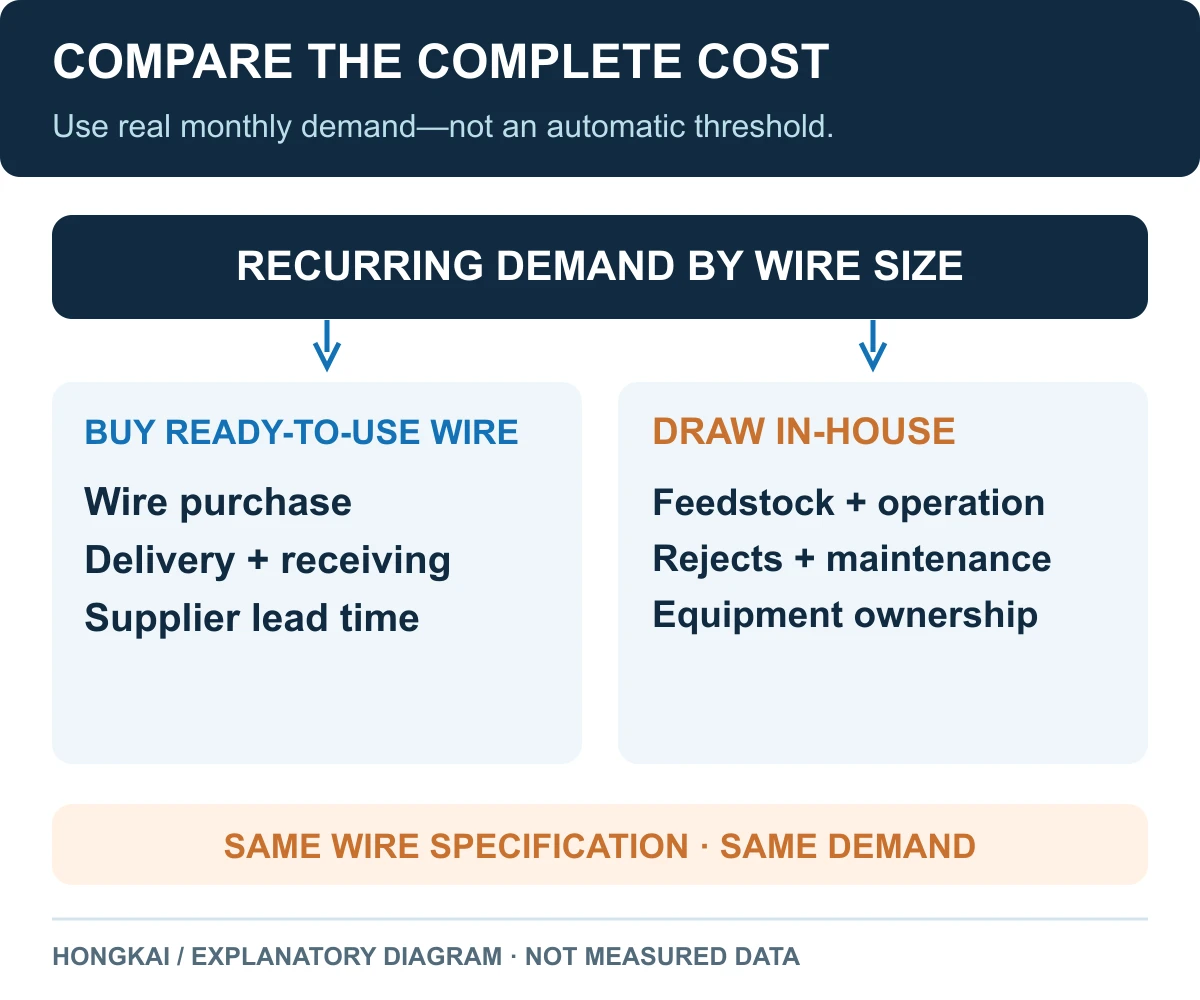
Planning diagram: compare complete costs under the same demand assumptions. This is not a break-even calculation or a savings claim.
Separate actual recurring demand from a hoped-for production target. Record how much wire the factory needs at each diameter, and whether that volume is steady or changes with individual orders. A large catalogue capacity is not useful if the factory cannot use the output.
Compare the delivered cost of ready-to-use copper wire with the cost of suitable feedstock plus drawing. Include labour, electricity, dies, drawing fluid, maintenance, rejected material and the cost of owning the equipment. Annealing, when required, also belongs in the comparison. Transport, waiting time and the cost of purchasing different sizes may matter, but their value must come from the factory’s actual purchasing records.
Buying wire remains a serious option when demand is uncertain or the full operating cost has not been established. Reaching the planning reference is a reason to obtain quotations and compare costs, not a reason to place an equipment order automatically. For a first network cable factory, the network cable business planning guide explains how orders and market demand should come before equipment selection.
Write Down the Required Wire Sizes and Starting Material
A drawing machine must match both the material fed into it and the wire required from it. Knowing only the finished diameter is not enough to choose a machine.
Write down the purchased material, its diameter and condition, the required final wire diameter, and the monthly quantity for each size. If those details are not yet known, first settle the wire specification rather than choosing between machine names.
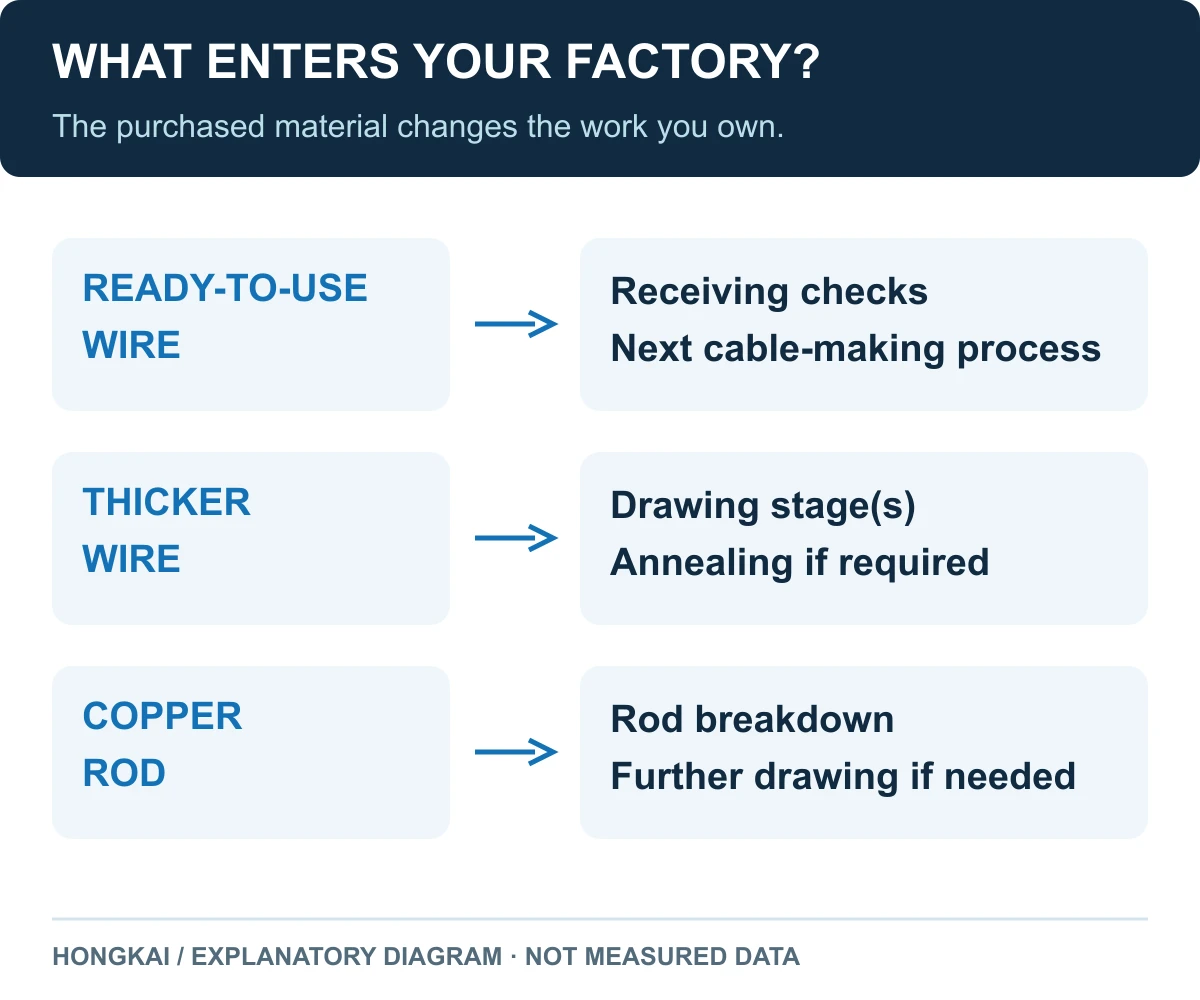
Simplified scope diagram, not a fixed line layout. Annealing and take-up requirements must be agreed for the selected route.
The following table separates three purchasing routes. It is not a fixed equipment list for every factory.
| What the factory buys | Work kept inside the factory | Main question before choosing |
|---|---|---|
| Copper wire already at the required diameter and condition | Receiving checks and the next cable-making process; drawing is outside this scope | Can the supplier reliably deliver the required wire, quantity and package? |
| Copper wire that still needs diameter reduction | The drawing stage or stages needed to reach the target, plus the agreed annealing and take-up scope | Does the selected machine accept the purchased wire and produce the required output? |
| Copper rod | Rod breakdown, with further drawing where needed for the final wire specification | Is the broader process justified by real demand, available skills and the full operating cost? |
Rod breakdown reduces rod into smaller wire. Further drawing may be required to reach the final size. Intermediate and fine drawing are useful machine categories, but their names alone do not specify a complete route. Manufacturer product ranges distinguish drawing machines, annealers and take-up equipment as separate parts of the production system.1
For a new factory, buying ready-to-use wire can be a practical starting point if there is a dependable source. Request the same written wire specification from the material supplier that you would use to accept wire from an in-house line. Buying wire transfers a process to a supplier; it does not remove the need to verify the output.
If a supplier proposes more than one drawing stage, ask what each stage receives and produces. For a stranded conductor, specify the diameter of the individual wires, not just the total conductor cross-section.
Do not assume that the words “intermediate” or “fine” have identical limits in every catalogue. Ask for a written operating range for the offered model and the exact route needed for your main products. HONGKAI’s intermediate drawing equipment reference is a starting point for that discussion, not confirmation of a project’s final configuration. A range that covers a small trial sample still needs to be checked against the planned production mix.
The input copper also matters. BECHEM’s technical guide identifies incoming rod quality and the drawing emulsion as important to the drawing process.2 Keep the feedstock supplier, material batch and actual input size in the trial record, so a change in the raw material is not confused with a change in machine performance.
Does the Finished Wire Need Annealing?
Drawing makes the wire smaller, but it also hardens the copper through deformation. Annealing is used to soften the drawn wire when the required finished condition calls for it. BECHEM’s technical guide describes this soft-annealing purpose and an inline drawing, annealing and spooling route.2 That example does not mean every purchase needs the same arrangement.

Decision illustration: specify the required wire condition before choosing the annealing scope. This is not an annealer setup instruction.
For a buyer, the useful question is what condition the next process or final product requires. Specify the required wire condition and applicable mechanical properties, such as elongation and tensile strength where the product specification calls for them. Do not describe acceptance only as “not brittle” or “soft enough”. Ask the supplier which tests will demonstrate the agreed condition.
The proposal should state whether annealing is included and where it occurs. Online or separate annealing must be selected for the actual route; this guide does not prescribe one arrangement. A drawing-only price and a drawing-and-annealing price do not cover the same work.
The finished package is another interface. Record the spool dimensions, usable loading requirement and the next machine’s pay-off arrangement. A spool that leaves the drawing line successfully still has to work at the insulation, bunching or other downstream process. For a bunched conductor, the wire bunching machine selection guide explains the input-wire and package information needed at that next stage.
Use one scope sheet for the drawing machine, annealing equipment, take-up, dies, cooling or fluid system, and required utilities. Mark each item as included, supplied separately or provided by the buyer. This is a scope comparison, not a claim that every project needs every accessory.
Compare Accepted Output, Not Only Metres per Minute
A line-speed figure tells you how quickly wire moves. It does not, by itself, tell you how much usable copper the factory produces during a shift. Wire diameter, number of wires, running time and rejected material all affect that comparison.
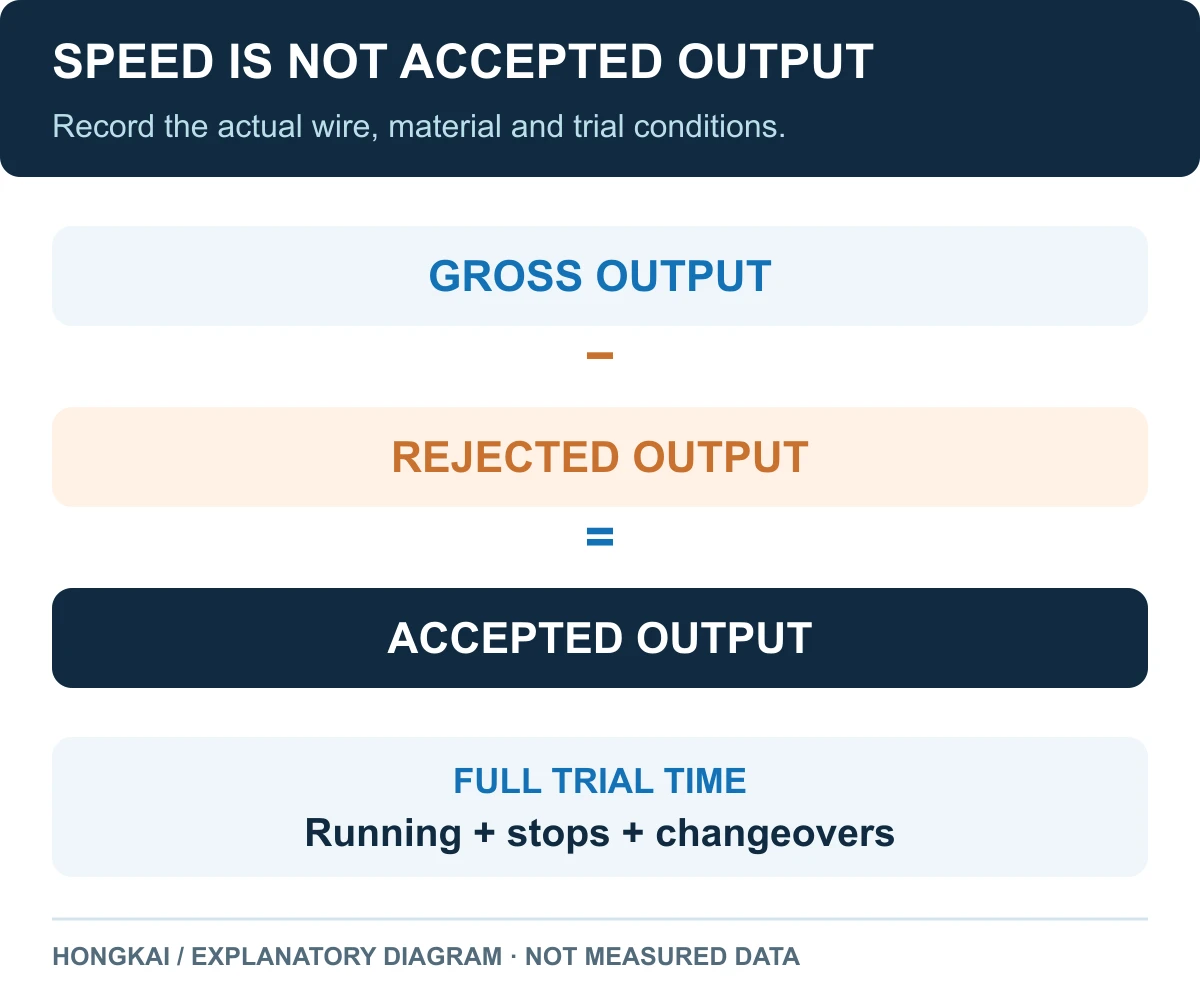
تصویر رکورد خروجی بدون نتایج نمونه. مقادیر را در همان واحد نگه دارید و نحوه شمارش مواد ردشده و بازکاریشده را توافق کنید.
Ask for an output record for the diameter and material you intend to run. Keep two figures separate: accepted output during stable running, and accepted output over the full agreed trial period. The second includes the effect of recorded stops and changeovers.
A useful comparison record contains:
- Input material and diameter, target wire diameter and number of wires being drawn.
- Actual running speed, elapsed trial time, stops and the reason for each stop.
- Gross output, rejected output and accepted output, with the weighing or counting method.
- The annealing arrangement and output spool used during the run.
These are proposed buyer records, not universal acceptance limits. Set the sample requirements and trial duration in the purchase agreement. If a supplier offers only a maximum speed without the associated product and test conditions, the factory still lacks the information needed for capacity planning.
Avoid assuming that one trial proves every diameter in a catalogue. Choose trial products that reflect the intended purchase, and agree how other sizes will be demonstrated.
Decide Which Responsibilities Your Factory Is Ready to Own
The final choice is a boundary decision. Buying finished wire keeps drawing with the material supplier. Buying intermediate wire brings part of that work inside. Starting with rod brings a wider processing route into the project.
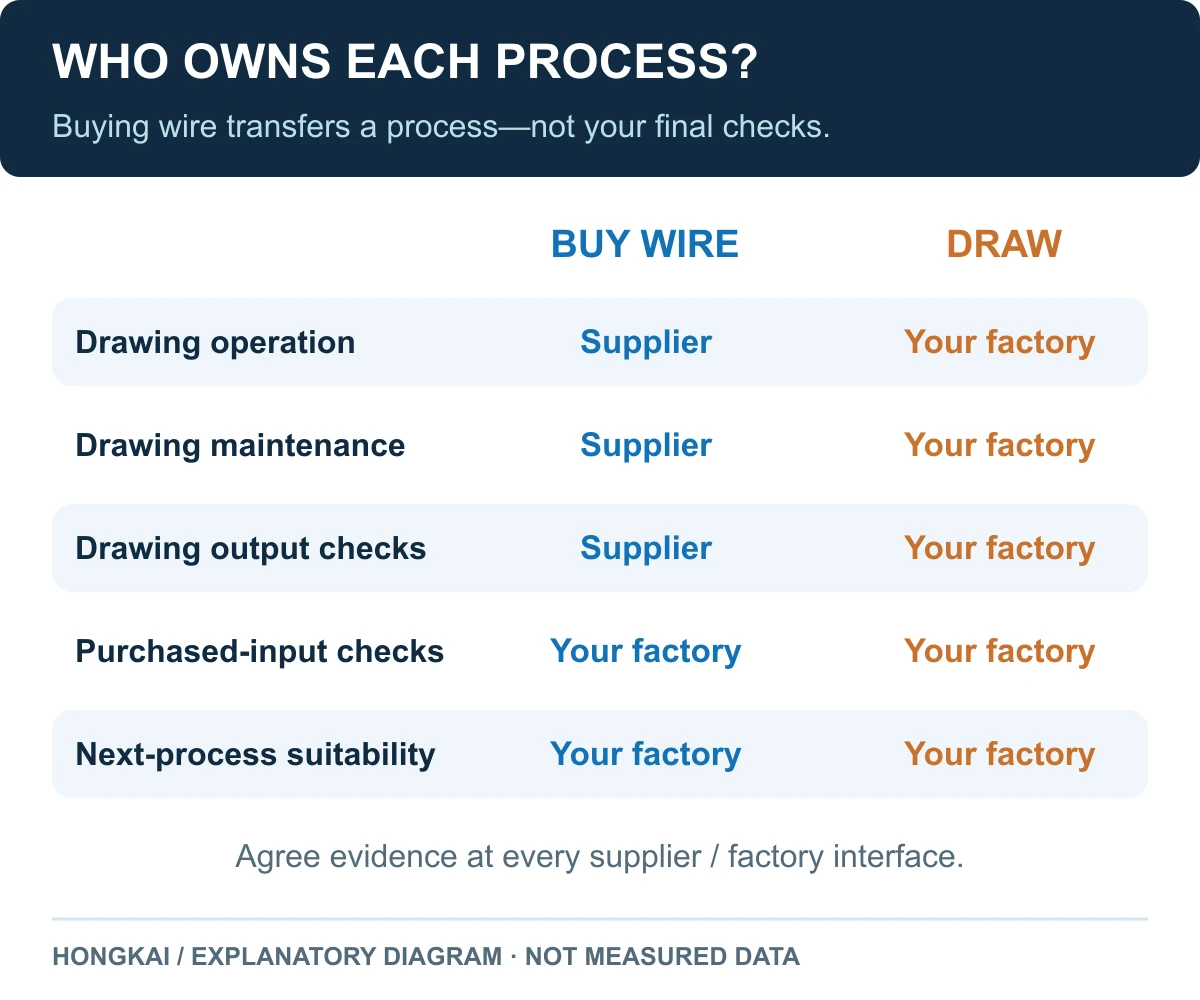
Simplified responsibility map for bought finished wire versus an in-house drawing stage. Both routes still need material and downstream-suitability checks.
Keep purchased wire as a serious option when demand is still uncertain or the factory has not yet budgeted for drawing operation and quality control. Evaluate an in-house stage when the product mix and material demand are clear enough to compare complete costs and responsibilities.
An in-house stage also needs a named owner for maintenance and spare parts. The cable-line maintenance planning guide helps define that responsibility; it is not a universal spare-parts list for every drawing machine.
Use the same wire specification and demand assumptions for both purchasing routes. Keep the supplier’s confirmed scope separate from options that still need a quotation. Neither an attractive machine price nor a generic savings percentage settles the make-or-buy decision.
Before accepting a drawing proposal, tie the trial results to the agreed finished-wire specification. Relevant items to define can include diameter, surface condition, electrical resistance and mechanical properties, together with the spool requirements. Select the actual tests and limits from the intended product specification, rather than borrowing numbers from an unrelated cable.
The result should be a clear decision: what copper enters the factory, what operations the factory owns, and what verified wire leaves those operations. Only then does comparing individual drawing machines become useful.
-
NIEHOFF product range distinguishes rod breakdown, single-wire and multiwire drawing, annealing and take-up equipment. This is a process-scope reference, not evidence of HONGKAI model performance. ↩
-
BECHEM, Lubrication solutions for wire drawing, printed pages 08–09, discusses incoming rod, drawing fluids and the drawing/annealing/spooling sequence. Its product-specific figures are not HONGKAI specifications. ↩ ↩