


A cable factory owner may be offered a single-screw extruder, a twin-screw extruder, or a proposal that uses both terms without defining the process boundary. The important decision is not whether two screws sound more advanced. It is whether the factory needs to apply an approved compound to a conductor or cable, manufacture the compound itself, or do both as separate production stages.
For most insulation and sheathing projects that begin with qualified cable compound, the main production duty is stable cable coating through a crosshead, supported by pay-off, preheating where required, cooling, measurement, testing, traction and take-up. Twin-screw equipment belongs primarily to a compounding process when the factory must feed, disperse, homogenize, vent and pelletize a formulation. A compounding line does not remove the need for a correctly specified cable-coating line.

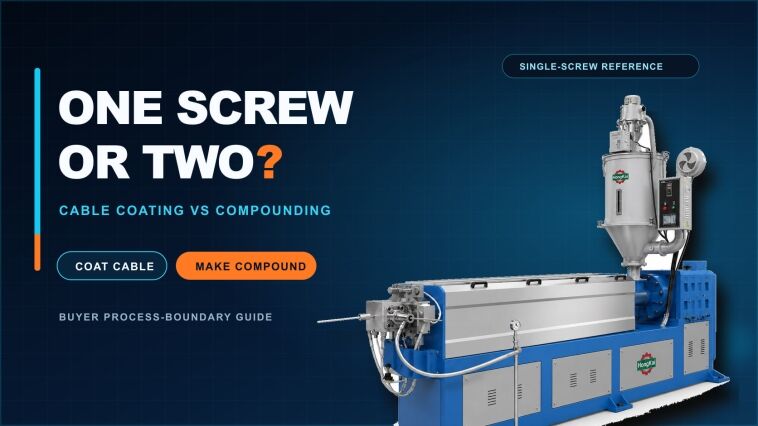
केबल-कोटिंग एक्सट्रूडर का HONGKAI संदर्भ रेंडर। छवि एक ट्विन-स्क्रू कंपाउंडिंग प्लांट को नहीं दर्शाती है या यह संकेत नहीं देती कि दोनों प्रक्रिया मार्ग एक-दूसरे के स्थान पर प्रयोग किए जा सकते हैं।.
This guide is for factory owners, production managers and technical procurement teams deciding what belongs in an extrusion quotation. It compares process duty, incoming material, finished output, auxiliary equipment and acceptance evidence so that screw count does not replace a complete production specification.
केबल कोटिंग को कंपाउंड निर्माण से अलग करें
A single-screw-versus-twin-screw comparison is meaningful only after the buyer states what enters the process and what must leave it. Applying insulation or sheath around a moving conductor is a different production boundary from turning polymers, fillers and additives into a controlled cable compound.
The cable-coating boundary starts with an approved material in a defined supply form. The material is prepared as required, melted and delivered through a crosshead around a conductor, insulated core or cable core. The output is a continuously coated wire or cable that must meet dimensional, surface, electrical and handling requirements.
The compounding boundary starts with a formulation and controlled ingredient streams. The process may include feeding, premixing, plasticizing, dispersive and distributive mixing, venting, filtration, pressure building, pelletizing, cooling and packaging. The output is normally an identified compound lot that still needs qualification and must later be processed on the cable extrusion line.
| Process boundary | सामान्य आगमन स्थिति | Required output | उपकरण को क्या साबित करना चाहिए |
|---|---|---|---|
| केबल इन्सुलेशन या शीथिंग | अनुमोदित पेलेट्स, ग्रैन्यूल या कोई अन्य आपूर्तिकर्ता-योग्य फीडस्टॉक | निर्दिष्ट पैकेज पर लेपित कंडक्टर या केबल | स्थिर आयाम, सतह, परत की अखंडता, आवश्यक ऑनलाइन जाँच और नियंत्रित टेक-अप |
| रंगीन पट्टी या एक अतिरिक्त केबल परत | अलग परत के लिए स्वीकृत सामग्री | केबल पर एक परिभाषित पट्टी या सह-निकाली गई परत | परत की स्थिति, निरंतरता, आयाम, प्रासंगिक स्थानों पर आसंजन और पुनरावृत्ति योग्य नियंत्रण |
| केबल-मिश्रण उत्पादन | एक सूत्र द्वारा परिभाषित नियंत्रित राल, भराव, योजक, तरल पदार्थ या पूर्व मिश्रण | योग्य पेलेट्स या अन्य अनुमोदित यौगिक रूप | सामग्री नियंत्रण, मिश्रण, वेंटिंग, तापीय इतिहास, बैच की एकरूपता और डाउनस्ट्रीम प्रक्रमणीयता |
| एकीकृत सामग्री और केबल परियोजना | कच्ची सामग्री तथा चालक या केबल इनपुट | योग्य कंपाउंड और एक अलग रूप से स्वीकृत तैयार केबल | दो जुड़े हुए लेकिन अलग-अलग रिलीज पैकेज: सामग्री प्रमाण और केबल प्रमाण |
The official Coperion cable-compound process illustrates the distinction clearly. Its two-stage system uses a twin-screw section for plasticizing, mixing and homogenizing, then a single discharge screw and pelletizing system for the compound-production duty.1 उस टैंडम सिस्टम में लगा एकल स्क्रू, केबल क्रॉसहेड लाइन जितनी उत्पादन सीमा नहीं रखता है, और कंपाउंड प्लांट से निकलने वाले पेलेट्स पूर्ण केबल नहीं होते।.
Decision criterion: Write one sentence for each proposed extruder: “This machine receives [named input] and produces [named output].” If the supplier cannot complete that sentence with a physical input, a controlled output and named acceptance evidence, the screw-count comparison is premature.
For HONGKAI cable-line scoping, the first practical input is the material the buyer intends to run. The material identity alone is still incomplete: the buyer must also state the cable construction and required output so that machine size and screw design can be reviewed together. A separate compounding review begins only when the project input is a formulation or multiple controlled ingredients rather than a ready-to-process cable compound.
दोनों मार्गों की तुलना समान आयामों पर करें
Single-screw cable coating and twin-screw compounding should be compared by process responsibility, not by a generic claim that one mixes better or runs faster. Each route is optimized around a different transformation and requires different upstream, downstream and quality systems.
| तुलना आयाम | एकल-स्क्रू केबल-लेपन रूट | दोहरी-स्क्रू कंपाउंडिंग प्रक्रिया |
|---|---|---|
| Primary duty | एक अनुमोदित मिश्रण को पिघलाएं और केबल क्रॉसहेड को लगातार आपूर्ति करें | एक परिभाषित मिश्रण प्रक्रिया के माध्यम से कई सूत्रीकरण सामग्रियों को संयोजित और नियंत्रित करें |
| मुख्य उत्पादन इनपुट | योग्य केबल यौगिक प्लस चालक, इन्सुलेटेड कोर या केबल कोर | राल, भराव सामग्री, एडिटिव्स, तरल पदार्थ, प्रीमिक्स या अन्य सूत्रीकरण इनपुट |
| मुख्य उत्पादन आउटपुट | इन्सुलेटेड तार, कोटेड कोर या शीथ केबल | बाद में केबल प्रसंस्करण के लिए कंपाउंड लॉट, सामान्यतः पेलेट्स |
| Mixing requirement | एक स्थिर मेल्ट बनाए रखें और अनुमोदित कंपाउंड को उसकी प्रक्रमण विंडो के भीतर संरक्षित करें | नियंत्रित सामग्री से निर्दिष्ट प्रकीर्णन, वितरण और समांगता बनाएं |
| दबाव और फॉर्मिंग ड्यूटी | एक क्रॉसहेड को फीड करें जो लगातार गतिमान केबल उत्पाद के चारों ओर एक परत बनाता है | एक डाई और डाउनस्ट्रीम कंपाउंड-हैंडलिंग या पेलेटाइज़िंग सिस्टम को फ़ीड करें; कुछ सिस्टम मिश्रण को दबाव निर्माण से अलग करते हैं |
| Essential surrounding equipment | आवश्यकतानुसार पे-ऑफ, सीधा करना या पूर्व-तापन, क्रॉसहेड और टूलिंग, शीतलन, गेज, टेस्टर, कैपस्टन, एक्यूमुलेटर और टेक-अप | Ingredient storage, accurate feeders, mixers where required, side feeding, liquid dosing, venting, filtration, pelletizing, cooling and lot handling |
| कोर स्वीकृति वस्तु | An identified cable sample made at a recorded stable condition | ट्रेसेबल सामग्री और नियंत्रित सूत्रीकरण से बना एक पहचाना गया यौगिक लॉट |
| Typical expansion question | क्या वही लाइन किसी अन्य स्वीकृत केबल निर्माण, सामग्री ग्रेड, परत या पैकेज को प्रोसेस कर सकती है? | Can the plant produce another qualified formulation without compromising feeding, mixing, venting, cleaning or lot control? |
यह विभेद तीन सामान्य नामकरण त्रुटियों को भी रोकता है।.
A current Maillefer component index maps screw-diameter extruders to insulation and sheathing duties across building wire, low-voltage, telecom, fiber-optic and other cable applications.2 वह संदर्भ केबल-कोटिंग सीमा का समर्थन करता है, लेकिन यह स्क्रू व्यास को अकेले चयन विधि नहीं बनाता है।.
First, a main extruder plus a small color-stripe extruder is not a twin-screw extruder. It is a multi-extruder cable line in which separate single-screw units feed different material streams or layers into compatible tooling.
In that arrangement, the main extruder and color-stripe extruder meet at the crosshead. The required stripe proportion is one of the inputs used to size the auxiliary extruder; the presence of two extruder bodies does not establish a twin-screw process.
Second, a multilayer crosshead supplied by two or three extruders does not make those extruders a twin-screw machine. The buyer must specify each layer, material, flow path, interface and control duty independently.
Third, a twin-screw feeder is not automatically a twin-screw process extruder. Ingredient feeding and polymer compounding are separate equipment functions, even when both use rotating screws.
Common mistakes: A quotation uses “double extruder,” “co-extrusion,” “twin screw” and “two-color line” as interchangeable terms. The buyer should require a process diagram that shows the number of extruder barrels, the screw arrangement inside each barrel, the material entering each unit and the die or crosshead receiving each melt stream.
सामग्री की स्थिति और विक्रय योग्य उत्पाद से मार्ग चुनें
The most reliable selection starts with the approved material supply strategy and the first saleable cable. A factory buying qualified compound needs a different project from a factory developing and manufacturing its own cable formulations.
मशीन मॉडल का अनुरोध करने से पहले इस अनुक्रम का उपयोग करें:
- पहली केबल निर्माण, परत क्रम, चालक या कोर इनपुट, समाप्त पैकेज और स्वीकृति आधार को फ्रीज़ करें।.
- प्रत्येक इन्सुलेशन, शीथ, स्ट्राइप या अन्य लगाई गई सामग्री को स्वीकृत ग्रेड और आपूर्ति रूप द्वारा नामित करें।.
- तय करें कि कारखाना योग्य कंपाउंड खरीदेगा, अपने यहाँ नियंत्रित कंपाउंड बनाएगा, या दोनों मार्गों का अलग-अलग मूल्यांकन करेगा।.
- आने वाली सामग्री से कंपाउंड लॉट तक और कंपाउंड लॉट से तैयार केबल तक प्रत्येक भौतिक परिवर्तन का मैपिंग करें।.
- Build separate factory acceptance test plans for any process boundary that creates a separately controlled output.
| Buyer situation | Preliminary route | सीमा जिसे अभी भी पुष्टि की आवश्यकता है |
|---|---|---|
| कारखाना अनुमोदित पेलेट्स खरीदता है और एक इंसुलेशन या शीथ परत लगाता है | अनुमोदित उत्पाद और सामग्री के चारों ओर केबल-कोटिंग लाइन निर्दिष्ट करें | पेंच डिज़ाइन, बैरल, क्रॉसहेड, टूलिंग, शीतलन और सहायक उपकरणों को सटीक सामग्री और केबल से मेल खाना चाहिए |
| केबल को एक रंगीन पट्टी या दूसरी सामग्री की धारा की आवश्यकता होती है | Review a separate auxiliary extruder and compatible crosshead or die arrangement | यह एकाधिक एक्सट्रूज़न ड्यूटी है, यह यह साबित करने का प्रमाण नहीं है कि ट्विन-स्क्रू प्रक्रिया की आवश्यकता है |
| The factory wants to blend resin, fillers and additives into its own commercial compound | Scope a dedicated compounding project before the cable line | फॉर्मूलेशन का स्वामित्व, फीडिंग, मिक्सिंग, वेंटिंग, पेलेटाइज़िंग, प्रयोगशाला मुक्ति और देयता लिखित होनी चाहिए |
| The factory wants to use reclaimed or variable material | केवल स्क्रू की संख्या के आधार पर चयन न करें | Input variability, contamination, filtration, degradation, qualification and finished-cable limits require a controlled development plan |
| परियोजना एक ताप-संवेदी, अत्यधिक भरित, प्रतिक्रियाशील, फोमित, रबर या क्रॉसलिंक करने योग्य प्रणाली का उपयोग करती है | Treat the process as material- and product-specific | सामग्री आपूर्तिकर्ता की प्रक्रमन आवश्यकताएँ प्राप्त करें और जहाँ लागू हो, निवास समय, अपरूपण, तापमान, वेंटिंग, वल्कनीकरण या फोमिंग नियंत्रण को परिभाषित करें |
| The supplier proposes one line for many PVC, PE, XLPE or low-smoke formulations | संगतता को अस्थायी रखें | Each exact compound grade, screw, tooling, dryer or loader need, cleaning route and acceptance sample must be reviewed |
“PVC,” “PE,” “XLPE” or “LSZH” is not a complete machine input. Commercial grades can differ in additives, fillers, moisture sensitivity, thermal limits, rheology, crosslinking route and required processing controls. A supplier should not convert a material family name into a universal screw geometry or output promise.
The HONGKAI project sequence is to match the required production output to a practical extruder size, then review the intended material against the screw design and the rest of the line. A dryer or additional feeding system is not added merely because the material name changes; those modules remain conditional on the exact grade, supply form and material-supplier processing guidance. The current Φ70 and Φ90 references therefore do not prove universal grade or brand compatibility.
The same caution applies to in-house formulation. Owning a twin-screw compounder creates responsibilities for recipes, ingredient verification, dosing accuracy, lot traceability, laboratory testing, change control, cleaning, nonconforming material and the interaction between compound quality and cable quality. It is a material-manufacturing decision, not merely an extra machine added to the extrusion hall.
Foaming and crosslinkable compounds require their own material-and-screw review because their raw-material behavior and test route differ from ordinary cable compounds. HONGKAI does not extend that confirmed boundary to recycled material or every high-fill low-smoke grade without the exact material data and a representative trial plan.
Red flags: A supplier recommends twin-screw equipment only because the buyer mentions additives; promises that “more mixing” will solve an undefined surface or electrical defect; or quotes a cable line before the compound grade, conductor, layer thickness, package and test basis are available.
पूरी लाइन निर्दिष्ट करें, केवल स्क्रू काउंट ही नहीं
A useful cable-extrusion quotation must connect the extruder to the conductor path, crosshead, cooling, measurement, traction, testing and take-up. A useful compounding quotation must connect raw-material control to feeding, mixing, venting, discharge, pelletizing, laboratory release and lot handling.
केबल-कोटिंग परियोजना के लिए, खरीदार को इन इनपुट्स के साथ एक उत्पाद-और-प्रक्रिया डॉसियर प्रदान करना चाहिए:
| Input group | तकनीकी समीक्षा के लिए न्यूनतम जानकारी |
|---|---|
| Finished cable | ड्रॉइंग, लेयर क्रम, नाममात्र और नियंत्रित आयाम, सतह आवश्यकता, अंकन और पैकेज |
| चालक या केबल कोर | सामग्री, निर्माण, आने वाला व्यास या सीमा, रील के आयाम, अनुमेय तनाव और सतह की स्थिति |
| Applied compound | आपूर्तिकर्ता और ग्रेड (जब उपलब्ध हो), आपूर्ति का रूप, रंग, प्रसंस्करण निर्देश, सुखाने या पूर्व-शर्त आवश्यकता और लॉट नियंत्रण |
| Extrusion duty | इन्सुलेशन, शीथ, बेडिंग, स्ट्राइप या कोई अन्य नामित परत; सामग्री स्ट्रीम्स की संख्या; टूलिंग अवधारणा; आवश्यक लाइन दिशा |
| Online control | व्यास या दीवार नियंत्रण विधि, जहां लागू हो, स्पार्क परीक्षण, मुद्रण या अंकन सत्यापन, लंबाई माप और ट्रेसेबिलिटी |
| Factory interface | बिजली, शीतलन जल, संपीड़ित वायु (जब आवश्यक हो), अपवाह, फर्श की योजना, उठाने और रील की गति, पर्यावरण नियंत्रण तथा मौजूदा उपकरण |
| Acceptance | उत्पाद लॉन्च, सामग्री के बैच, लक्षित संचालन स्थिति, माप, परीक्षण विधियाँ, संरक्षित रिकॉर्ड और अनसुलझे मदों की प्रक्रिया |
HONGKAI’s verified Φ70 insulation-line and Φ90+50 sheathing-line configuration documents show single-screw cable-coating references with separate material handling, crosshead, cooling, measurement, traction and take-up functions. The “+35” or “+50” designation in these references identifies an additional color-stripe extruder; it does not describe an intermeshing twin-screw barrel. Final screw, barrel, tooling, material and line scope remain project-specific.
For a color-stripe request, the buyer should also define the stripe proportion and visible result. That input affects the auxiliary-extruder size and crosshead arrangement; it should not be translated into a generic request for a “twin-screw cable extruder.”
सार्वजनिक HONGKAI केबल शीथिंग लाइन इसी प्रकार, एक्सट्रूडर को एक लंबी लाइन के भीतर एक स्टेशन के रूप में प्रस्तुत करता है जिसमें पे-ऑफ, क्रॉसहेड, शीतलन, व्यास माप, ट्रैक्शन और टेक-अप शामिल हैं। HONGKAI कम वोल्टेज उत्पादन गाइड अनुमोदित केबल परतों और आवश्यक मार्ग से शुरू होता है, न कि एक एक्सट्रूडर मॉडल को पूर्ण कारखाने के रूप में मानना।.
रखरखाव या प्रतिस्थापन कार्य के लिए, HONGKAI केबल एक्सट्रूज़न पार्ट्स पेज lists the measurements needed to confirm a screw and barrel, including diameter, length or L/D information, thread form and material requirement. Those replacement inputs are also useful during a new-line review, but dimensional compatibility alone still does not prove process suitability.
Note: Current HONGKAI evidence supports the cited single-screw cable-coating configurations. It does not by itself establish a HONGKAI twin-screw compounding model, formulation package or compound-performance guarantee. Any in-house compounding scope must identify the responsible specialist, formulation owner, supplied modules and acceptance boundary in writing.
कंपाउंड और केबल के लिए अलग-अलग FAT प्रमाण तैयार करें
Factory acceptance should prove the output of each production boundary. A compounder must release an identified material lot against the agreed formulation and test plan; a cable line must run an identified product at a stable recorded condition and release the cable against the agreed dimensional, electrical, mechanical and handling checks.
| Evidence layer | केबल-कोटिंग लाइन FAT | कंपाउंडिंग-लाइन FAT |
|---|---|---|
| Controlled inputs | अनुमोदित चालक या केबल कोर, कंपाउंड लॉट, टूलिंग और पैकेज | अनुमोदित सूत्रीकरण संशोधन, सामग्री के बैच, फीडर और मात्रा अभिलेख |
| Process record | तापमान क्षेत्र, स्क्रू और लाइन की स्थिति, पिघलने या प्रक्रिया अवलोकन, ट्रैक्शन, शीतलन और संबंधित अलार्म | फ़ीड दर, स्क्रू कॉन्फ़िगरेशन और स्थिति, तापमान, टॉर्क या लोड, वेंटिंग, दबाव, फ़िल्ट्रेशन और जहाँ लागू हो, पेलेटाइज़िंग की स्थितियाँ |
| Physical output | सहमत रील या पैकेज पर पहचानित इंसुलेटेड या शीथ वाला केबल | सहमत पेलेट या सामग्री रूप में पहचाना गया यौगिक लॉट |
| Immediate checks | आयाम, समकेन्द्रता या आवश्यकता होने पर भित्ति का प्रमाण, सतह, अंकन, ऑनलाइन परीक्षण और वाइंडिंग की गुणवत्ता | उपस्थिति, पेलेट या आउटपुट स्थिरता, संदूषण नियंत्रण और सहमत प्रयोगशाला नमूना पहचान |
| Release evidence | केबल ड्रॉइंग, मानक या नियंत्रण योजना से जुड़े उत्पाद-विशिष्ट परीक्षण | सामग्री परीक्षण सूत्र विनिर्देश और डाउनस्ट्रीम प्रसंस्करण आवश्यकता से जुड़े हुए |
| Traceability | केबल रील से कंडक्टर/कोर, कंपाउंड लॉट, सेटिंग्स, परीक्षण और ऑपरेटर रिकॉर्ड तक | संयुक्त लॉट से सामग्री, सूत्रीकरण संशोधन, सेटिंग्स, नमूने, परीक्षण और निपटान तक |
| Handover | Recipes or settings as agreed, tooling list, drawings, manuals, alarms, training and open items | Formulation responsibility, screw configuration record, feeder calibration, cleaning/changeover method, lab methods, traceability and open items |
Open-head output is not enough to accept a cable line. It does not prove that the selected conductor, crosshead, tooling, cooling path, measurement system, traction and take-up can produce the agreed cable continuously. Likewise, a short cable sample cannot prove a compound plant if ingredient control, lot uniformity, venting, filtration, pellet condition and laboratory release remain undefined.
HONGKAI uses two different checks for the cable-extrusion duty. First, the head is opened and the extruder output is weighed under the agreed full-speed test condition to record kilograms per hour. Second, the complete line runs the customer’s specified cable under the agreed full-speed condition to record metres per minute while the finished dimensions and other signed accuracy requirements remain within tolerance. The first check verifies extrusion output; the second verifies that the complete line can make the agreed product. Neither result should substitute for the other.
खरीदार यह अंतिम स्क्रीनिंग चेकलिस्ट का उपयोग दोनों मार्गों में से किसी एक को मंजूरी देने से पहले कर सकता है:
- ☐ प्रत्येक एक्सट्रूडर के लिए प्रक्रिया इनपुट और आउटपुट का नामकरण किया गया है।.
- ☐ “सिंगल,” “ट्विन,” “को-एक्सट्रूज़न” और “कलर स्ट्राइप” का उपयोग प्रक्रिया आरेख और उपकरण सूची में सुसंगत रूप से किया गया है।.
- ☐ सटीक सामग्री ग्रेड या नियंत्रित सूत्रीकरण, सामान्य पॉलीमर-परिवार के शब्दों को प्रतिस्थापित करता है।.
- ☐ Upstream and downstream modules are included with their interfaces and responsible supplier.
- ☐ Cable-coating FAT and compound-production FAT have separate samples, records and release criteria.
- ☐ भविष्य की सामग्री या केबल परिवारों को वैकल्पिक दायरे के रूप में सूचीबद्ध किया जाता है जब तक कि प्रतिनिधि परीक्षण और साक्ष्य सहमत न हो जाएँ।.
- ☐ HONGKAI-manufactured equipment, integrated specialist equipment and buyer-supplied systems are separated in the responsibility matrix.
The correct choice is therefore not “single screw or twin screw” in isolation. It is a verified route from the buyer’s material state to the first saleable cable, with every transformation, interface and acceptance record assigned to the correct production boundary. Twin-screw compounding is included here as buyer education, not as evidence of a current HONGKAI compounding-machine offer. If a project includes pellet production, the specialist compound-equipment and formulation scope must be defined separately from the HONGKAI cable-coating line. The same input dossier can be submitted through the clean HONGKAI परियोजना इंटेक पृष्ठ so that cable coating, material preparation and any specialist compounding scope are reviewed separately.
-
Coperion, केबल कंपाउंड के लिए STS Mc11 दो-चरणीय कंपाउंडर, describes feeding, twin-screw mixing and homogenizing, transfer to a single discharge screw, and pelletizing as one cable-compound production system. ↩
-
Maillefer, तार और केबल इन्सुलेशन और शीथिंग के लिए एक्सट्रूडर, केबल इन्सुलेशन और शीथिंग अनुप्रयोगों में उपयोग किए जाने वाले स्क्रू-आधारित एक्सट्रूडरों के लिए एक वर्तमान निर्माता संदर्भ प्रदान करता है; अंतिम स्क्रू और लाइन चयन अनुप्रयोग-विशिष्ट बना रहता है। ↩
