• Home
  • About
    • PRODUCTS & PRODUCTION

      Find your next production step.
      Production lines

      Start with the cable you want to make.

      Equipment for optical cable manufacture

      Equipment for twisted-pair cable

      Machinery for insulated wire and cable

      Spare Parts & Support

      Replacement parts for HONGKAI machinery.

      Explore parts by production line

      Check photos, nameplates and part numbers

      Send machine details, photos and quantity

      Cable & materials

      Explore cable structures and inputs.

      Browse fiber optic cable types

      Materials for optical cable production

  • BLOG
  • Contact

CAT6A / CAT7 Cable Production Line

A project-based configuration with insulation, foaming, taping and braiding routes.

PRODUCTION LINE PREVIEW

Reference configuration

SHIELDED CONSTRUCTION REVIEW

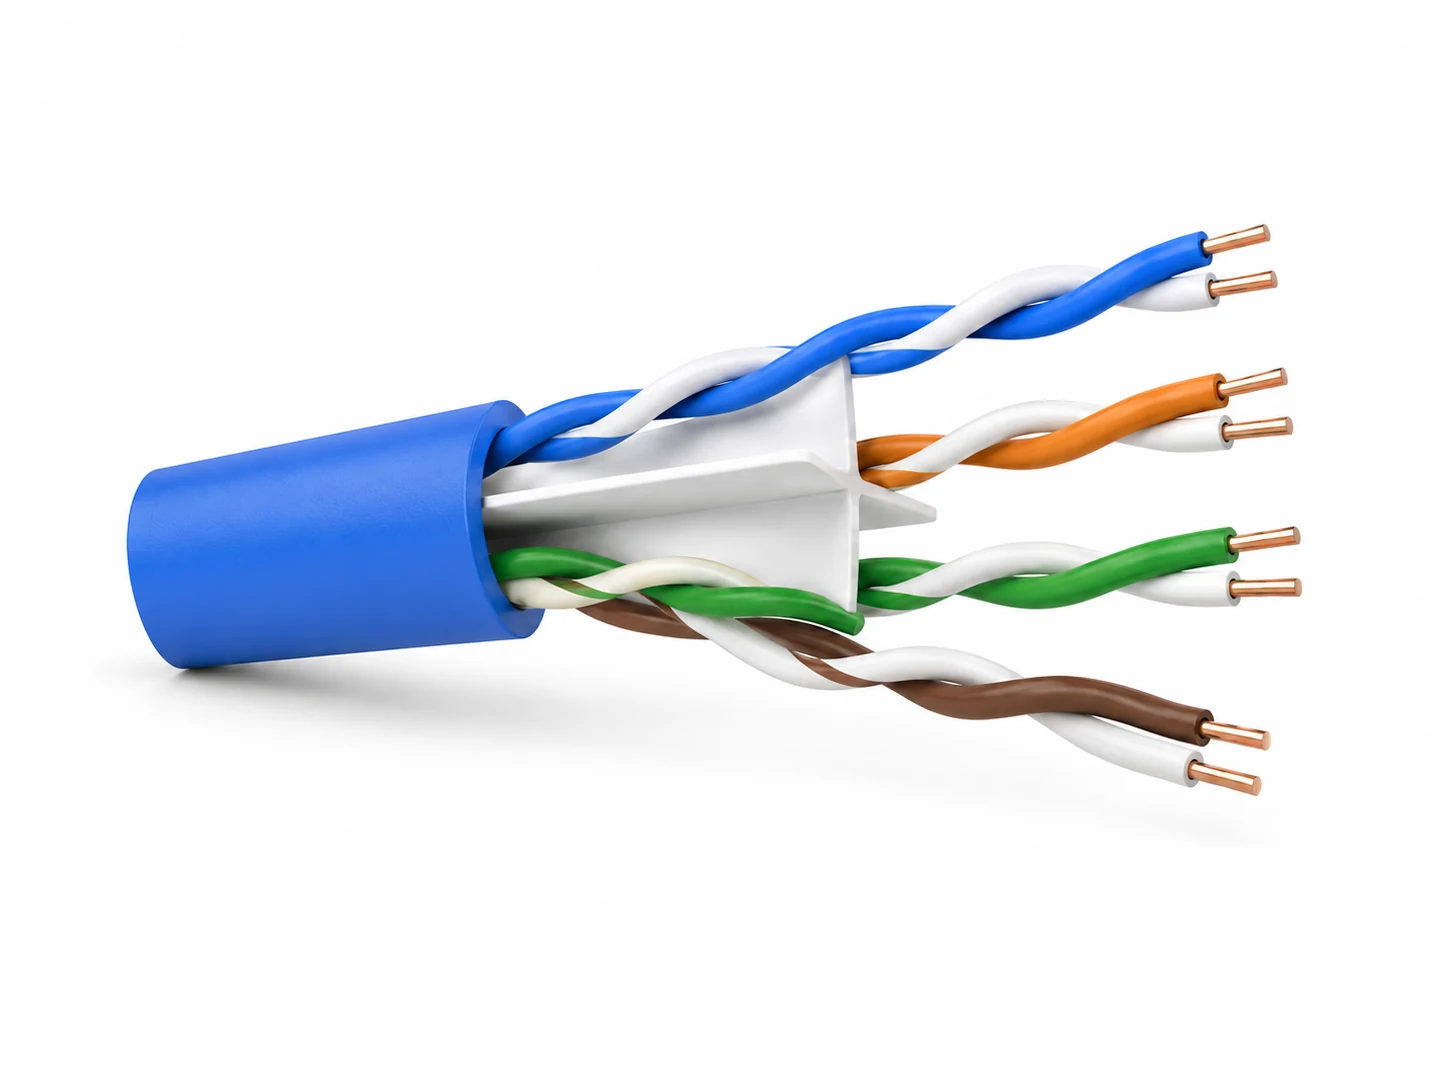
4 PAIRS · FOIL & BRAID S/FTP construction with individually screened pairs and an overall braid. Confirm the foil path and shielding from the approved cable drawing.
S/FTP cable construction with four individually foil-screened twisted pairs and an overall braid.
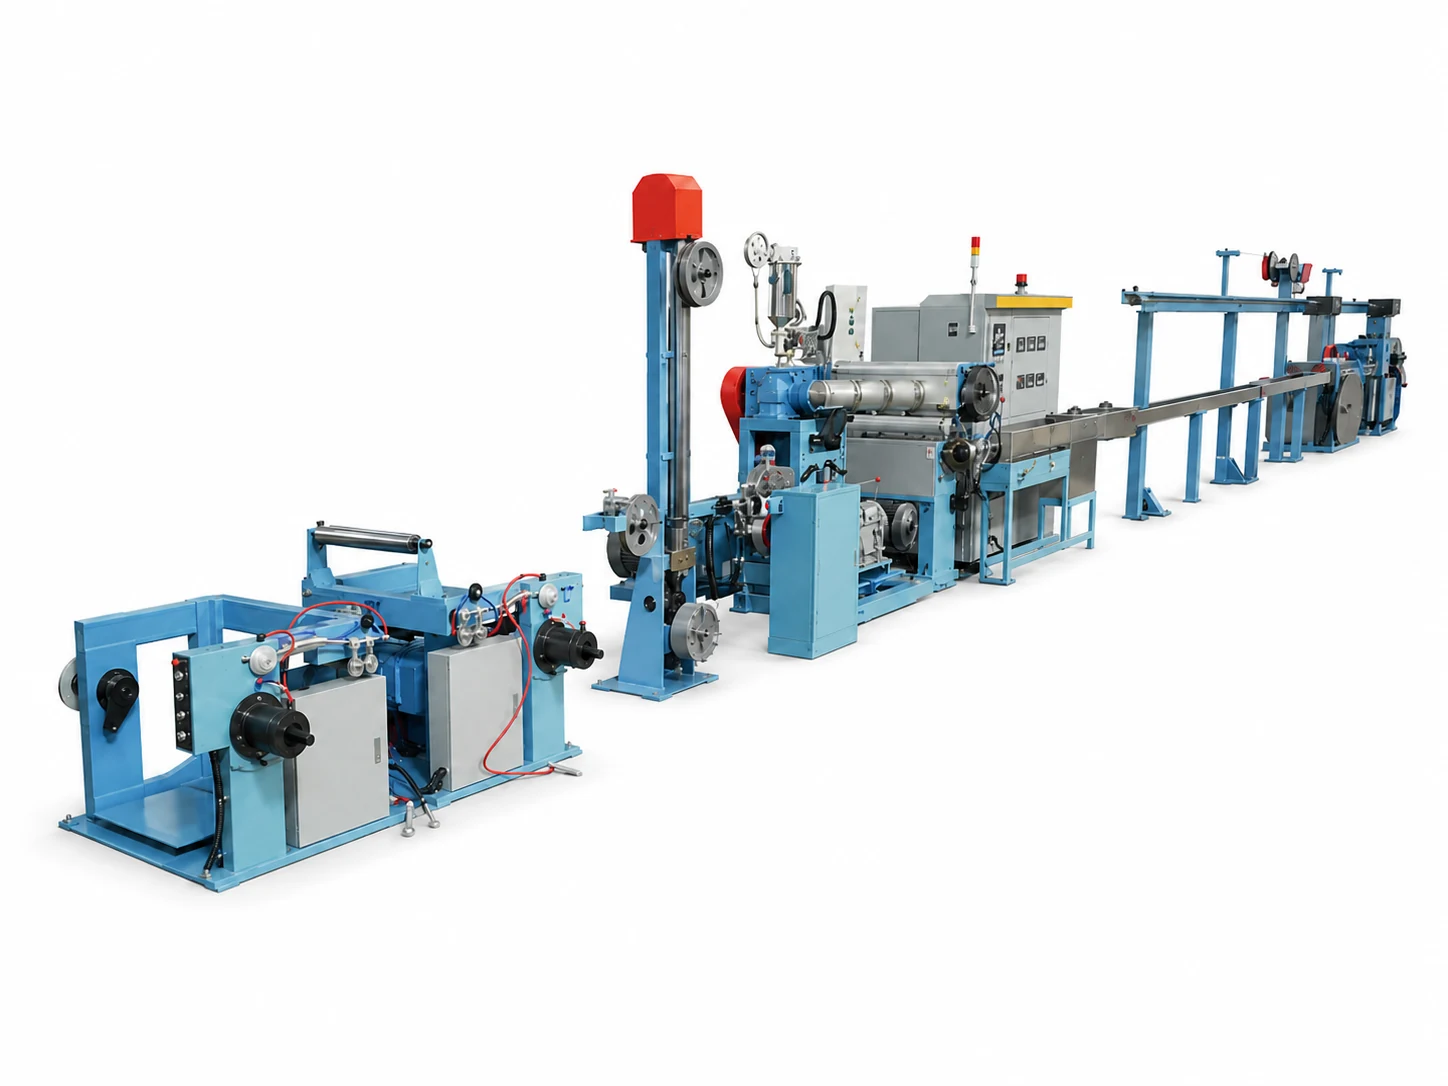
Physical-Foaming Tandem LinePhysical-Foaming Tandem Line
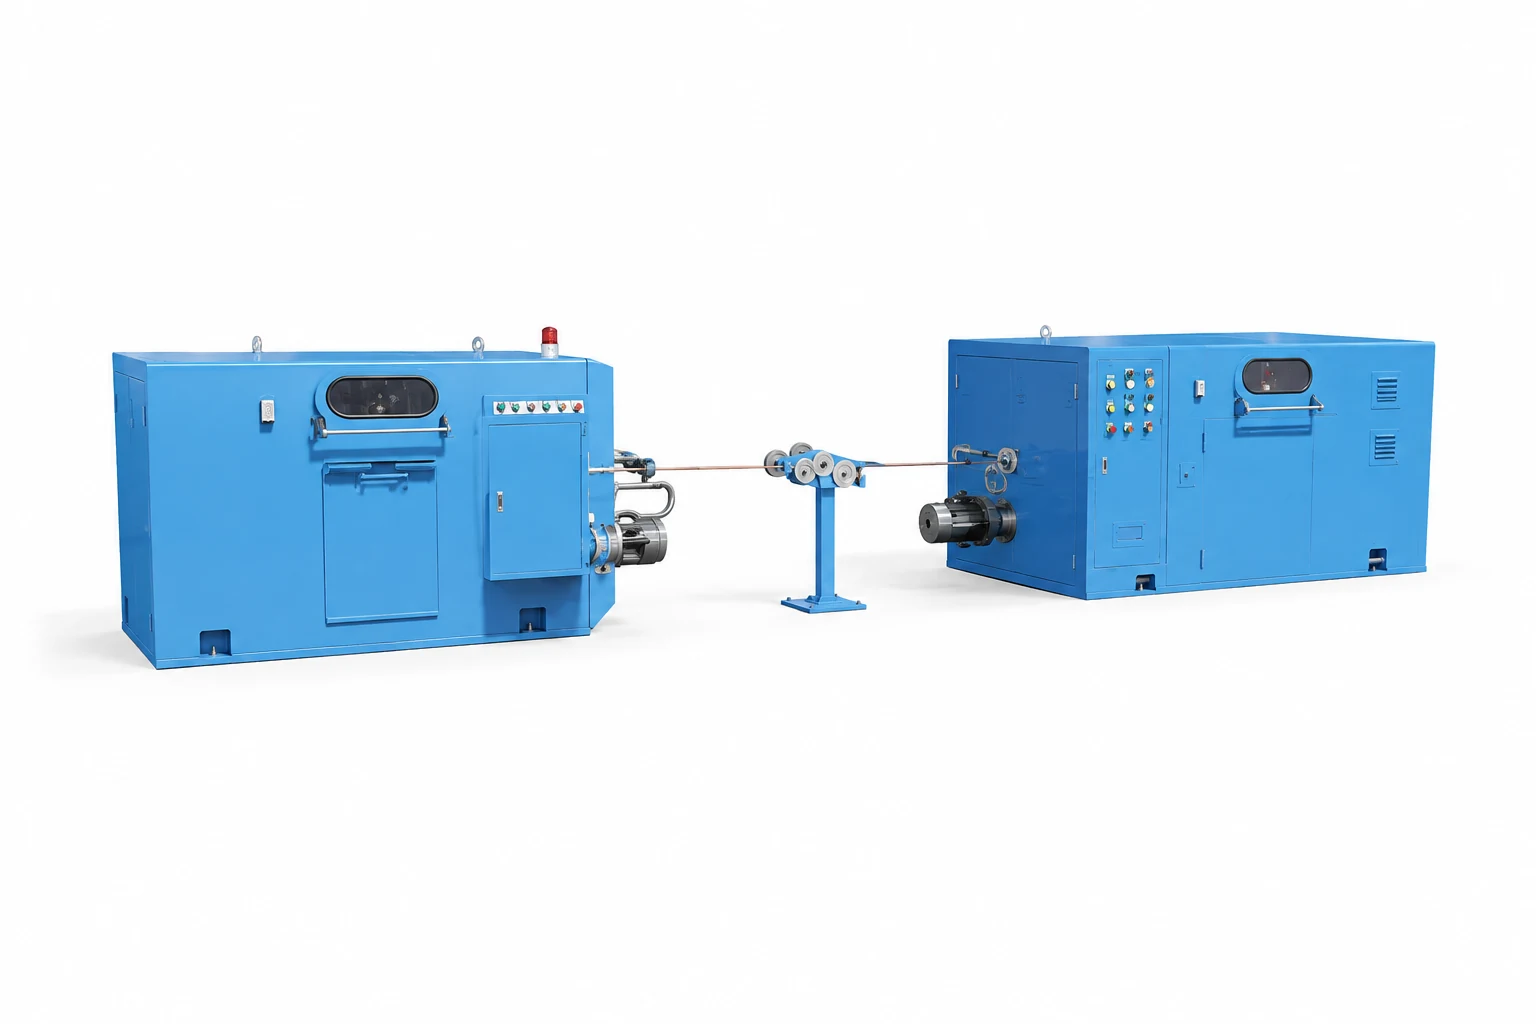
500 Back-Twist Pairing System500 Back-Twist Pairing System
800 Cantilever Cabling & Taping800 Cantilever Cabling & Taping
24-Carrier Metal Braiding Machine24-Carrier Metal Braiding Machine
80 Outer-Sheathing Line80 Outer-Sheathing Line
PRODUCTION DETAILS BELOWReview the process and equipment modules
REFERENCE PROJECT SCOPE CAT6A / CAT7 Cable Production Line Specification-led · Reference configuration
What does this production line produce?

Plan a CAT6A or CAT7 LAN cable project around the supplied eight-family equipment schedule. Review solid insulation and physical foaming, separator production, back-twist pairing, cabling and taping, metal braiding, sheathing and coiling. The final route follows your cable drawing and acceptance plan.

Product range
CAT6A / CAT7 · drawing-led configuration
Control priority
Dielectric geometry, shielding and electrical tests
Main process
Insulation → pairing → screening → jacket
Acceptance basis
Approved cable specification or sample

Start with Your LAN Cable Specification

Machine selection is the result of the required cable, not the starting point.

STEP 01 · PROJECT INTENT

What are you planning?

Changes the questions we ask, not an automatic machine claim.
STEP 02 · PRODUCT DEFINITION

Define the cable before the machines

Choose known inputs and leave uncertain items for joint confirmation.

Open the cable before choosing the process

Select a layer to see its function, manufacturing stage and control responsibility.

Compare shielding structures. Final construction follows the approved cable drawing.
FOUR-PAIR SHIELDED CONSTRUCTIONFINAL DRAWING CONTROLS THE PROJECT
S/FTP cable construction with four individually foil-screened twisted pairs and an overall braid.

SELECTED LAYER · 03

Four twisted pairs

This is the key process relationship behind crosstalk control; final values follow the approved cable design.

Layer function
Uses controlled pair geometry to manage interaction between signal pairs.
Manufacturing process
Pair twisting, back-twist planning and four-pair cabling
Key control
Pair-specific lay length, tension, back-twist and deformation

Every process stage protects cable performance

Seven process decisions connect the source equipment schedule to the finished cable. Separator and shielding stages follow the selected design.

Equipment configuration

Insulation / physical foaming
STEP 01

Insulation / physical foaming

Choose between the 60+35 insulation route and the physical-foaming tandem route after confirming the dielectric system. The source foaming details discuss FEP; a different compound needs qualification.

Input
Approved copper wire + insulation compound
Output
Insulated core ready for pairing
Related equipment
60+35 insulation / physical-foaming tandem
KEY CONTROLDiameter, concentricity and qualified dielectric process
ENGINEERING CHECKPOINTS
  • Compound and tooling
  • Online dimensional monitoring
  • Foaming operating point, when applicable

Electrical results are built through the process

Confirm the CAT6A or CAT7 test basis and cable drawing before setting process controls.

Conductor & insulation

INFLUENCES Resistance / insulation consistency

Conductor dimensions, concentricity and the approved solid or foamed insulation structure

Pair twisting

INFLUENCES Crosstalk behaviour

Pair-specific lay, back-twist settings, tension and geometry repeatability

Cabling & shielding

INFLUENCES Core / shield consistency

Assembly tension, approved separator position, foil path and braid coverage

Sheathing

INFLUENCES Finished dimensions

Jacket thickness, cooling and surface quality

Taping and braiding modules do not by themselves establish an S/FTP construction. Confirm each pair-foil path, overall shield, drain wire where specified and the final electrical acceptance tests.

Eight equipment families. One coordinated project.

The quantities below reproduce the supplied project schedule. They are a reference allocation, not a fixed minimum for every CAT6A or CAT7 factory.

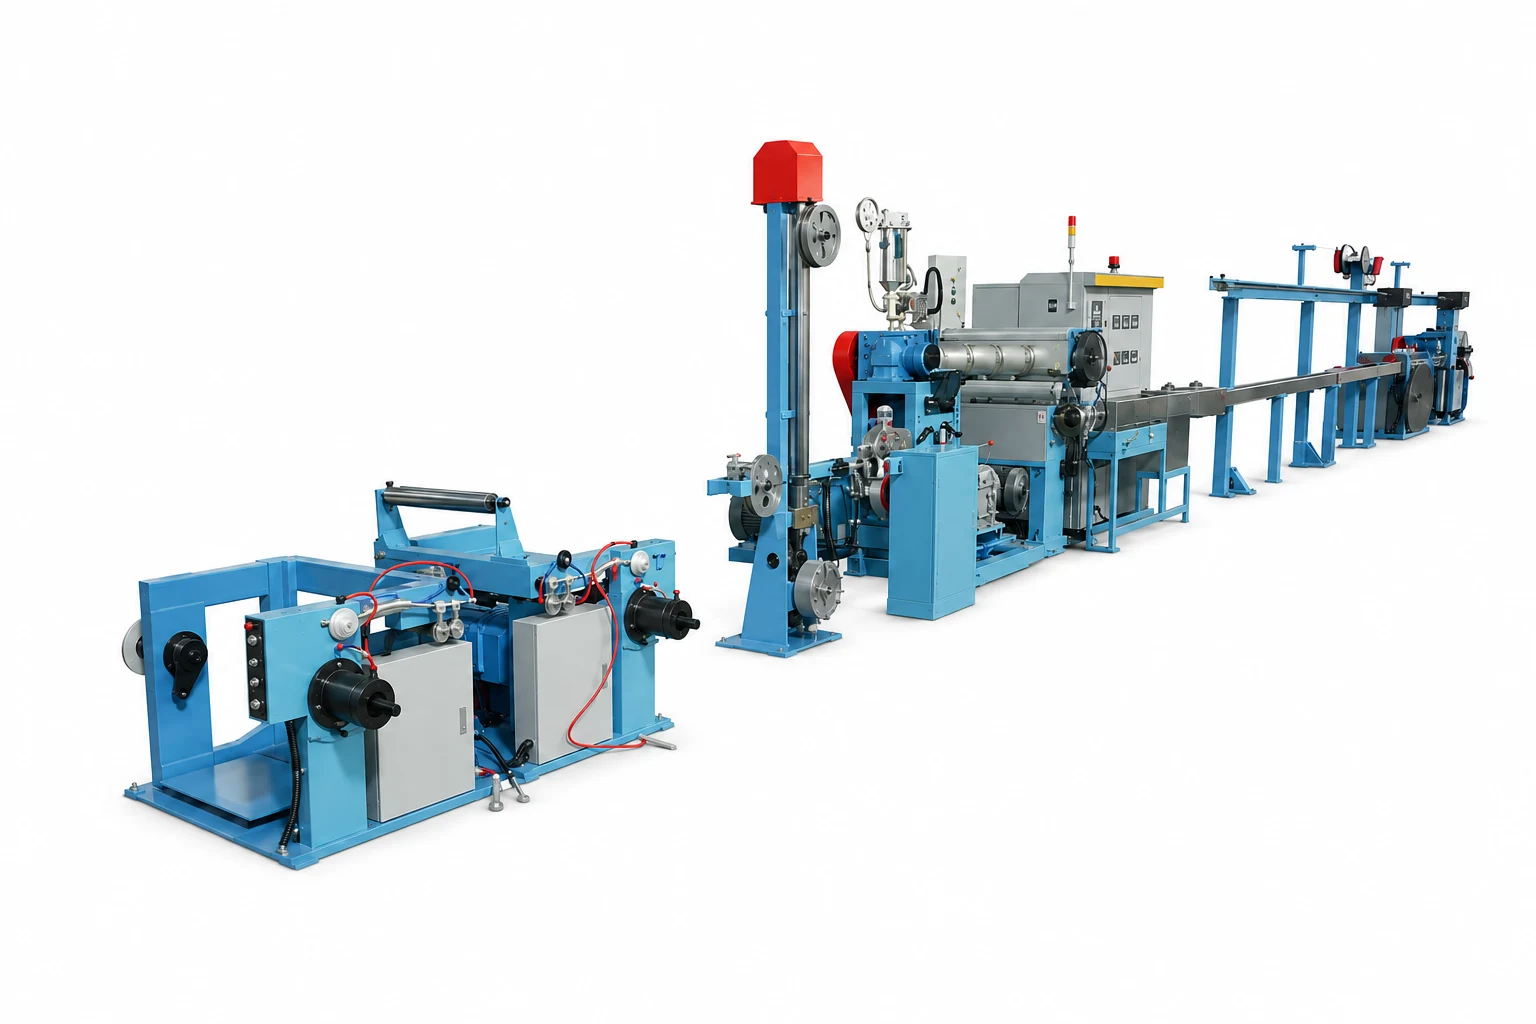
0160+35 High-Speed Insulation Line

60+35 High-Speed Insulation Line

Produces colour-identified insulated cores with conductor preparation, extrusion, cooling and online monitoring.

1 set · source allocation View equipment family
02HK-50 Cross-Separator Line

HK-50 Cross-Separator Line

Extrudes a plastic cross separator as a separate upstream material stream where the cable drawing requires it.

1 set · source allocation
03Physical-Foaming Tandem Line

Physical-Foaming Tandem Line

Combines drawing, annealing, insulation extrusion and nitrogen injection in the documented foaming route.

1 set · source allocation
04500 Back-Twist Pairing System

500 Back-Twist Pairing System

Pairs the insulated conductors with back-twist payoff and controlled tension before four-pair assembly.

8 sets · source allocation View equipment family
05800 Cantilever Cabling & Taping

800 Cantilever Cabling & Taping

Assembles the four pairs. The documented package includes pair-to-pair active taping, centre wrapping and side wrapping.

2 sets · source allocation View equipment family
0624-Carrier Metal Braiding Machine

24-Carrier Metal Braiding Machine

Applies a metallic braid around the assembled core when an overall braided screen is specified.

10 sets · source allocation
0780 Outer-Sheathing Line

80 Outer-Sheathing Line

Applies the approved jacket to the assembled cable core, then cools, checks and takes up the finished cable.

1 set · source allocation View equipment family
08500 LAN Cable Coiling Machine

500 LAN Cable Coiling Machine

Winds finished network cable into the agreed coil format for subsequent packing.

1 set · source allocation View equipment family

Equipment configuration

SELECTED MODULE · 01 60+35 High-Speed Insulation Line

PROCESS-TO-EQUIPMENT MAPPING

60+35 High-Speed Insulation Line

Produces colour-identified insulated cores with conductor preparation, extrusion, cooling and online monitoring.

Receives
Copper conductor + approved insulation compound
Delivers
Insulated core wire
Project decision
Confirm conductor range, compound, die tooling and the operating point for the approved cable.
1 set in the source project schedule Place this module in a configuration

Equipment configuration · final equipment and construction subject to project approval.

Source project allocation · quantities and operating references
EquipmentQuantitySource speed entrySpecification pages
60+35 High-Speed Insulation Line1 set800–1,000 m/min · schedule reference3–11
HK-50 Cross-Separator Line1 set120 / 450 m/min · conflicting source entries12–18
Physical-Foaming Tandem Line1 setFoaming 500; core wire 1,000; design 1,200 m/min · p.2819–29
500 Back-Twist Pairing System8 sets33–65 m/min · schedule reference30–32
800 Cantilever Cabling & Taping2 sets60 m/min schedule; 15–118 m/min detailed range33–35
24-Carrier Metal Braiding Machine10 sets5 m/min schedule; 329 m/h detailed reference36
80 Outer-Sheathing Line1 set120 m/min schedule; 100 m/min detailed line rating37–44
500 LAN Cable Coiling Machine1 set150 m/min schedule; 120 m/min in both detailed alternatives45–50

Source: Cat6/6E/7 Production Line Full Project, 50 pages; page 2 contains the allocation / rate schedule. Its 6E title is not CAT6A certification. Machine design speeds, operating modes and whole-factory output are different measures. Resolve the separator, sheathing and winding rate differences before quotation.

Choose a starting point, then engineer the details

Use the source project as a reference, then select the correct route for your CAT6A or CAT7 cable.

SOURCE PROJECT CONFIGURATION

The supplied schedule combines eight equipment families and 25 allocated sets. This is the documented project baseline, subject to scope and capacity review.

  • 1 insulation line + 1 separator line + 1 foaming tandem line
  • 8 back-twist pairing systems + 2 cantilever cabling packages
  • 10 metal braiding machines
  • 1 outer-sheathing line + 1 network-cable coiler
  • Clarify foil paths, compound qualification and finished-cable test equipment
Discuss this configuration

Request a project quotation after confirming the cable drawing, equipment allocation, testing scope and commercial terms.

Protect the next production decision

Plan the intended CAT6A / CAT7 constructions first. Changes to insulation, pair shielding or braid construction need a fresh tooling, material and capacity review.

  • Product range

    Reserve space for the approved solid or foamed insulation route, separator handling, taping and braiding requirements.

  • Factory flow

    Plan reel buffers, access and material flow between extrusion, pair twisting, cabling, braiding and coiling.

  • Utilities & controls

    Confirm power, cooling, air, ventilation and control interfaces against the selected compounds and machine scope.

Illustrative LAN cable factory planning layout
ILLUSTRATIVE LAYOUT · NOT THE EIGHT-FAMILY EQUIPMENT PLAN

What changes the equipment solution?

Use the equipment schedule as a starting point. Confirm these inputs before fixing the CAT6A / CAT7 route.

Cable specification

Category, conductor, solid or foamed insulation, pair foil, overall shield, separator and jacket requirements

Performance target

Project test standard, frequency range, limits, shield checks and instrument capability

Output & automation

Product mix, batch sizes, reel transfers, operators, changeover and packing format

Factory conditions

Clear dimensions, utilities, ventilation, reel-buffer space and installation access

Build the acceptance plan before the line is finalized

Match production checks and finished-cable tests to the approved CAT6A / CAT7 construction.

Illustrative LAN cable connected to a generic tester and remote unit; this is not a CAT6A or CAT7 acceptance test record
ILLUSTRATIVE LAN TESTING SCENE · NOT A CAT6A / CAT7 TEST RECORD
SELECTED QUALITY VIEW

In-process control

Controls that protect repeatability while the cable is being made.

01
Insulation structure

Diameter, concentricity and approved solid or foamed structure

Confirmed compound, tooling and inspection method
02
Pair formation

Pair-specific lay, back-twist, tension and geometry

Pair setup and sample confirmation
03
Core & shielding

Separator position, pair-foil path, taping, braid and specified drain-wire checks

Approved drawing and recorded shield construction
04
Outer jacket

Thickness, finished diameter, surface and marking

In-line and final visual/dimensional record
Add test requirements

Avoid decisions that create unstable cable later

Resolve material, shielding and capacity assumptions before approving the equipment configuration.

Selecting by nominal speed only

Core-wire, foaming and design speeds describe different conditions. None is a guaranteed output for the complete production route.

Assuming taping plus braid proves S/FTP

The listed taping functions do not yet confirm four independent pair-foil paths. Match the actual foil route to the approved cable drawing.

Treating equipment quantities as line balance

Eight pair-twisting units and ten braiding units are schedule quantities. Batch sizes, reel buffers, changeovers and tested output still require capacity planning.

Know who is responsible for each part of the solution

Confirm models, quantities, tooling, interfaces and test responsibilities in the final technical proposal.

CORE EQUIPMENT Manufactured by HONGKAI

The agreed machinery scope must identify each extrusion, twisting, cabling, taping, braiding and coiling module.

SOLUTION SCOPE Configured & supplied by HONGKAI

Confirm separator tooling, foam-system interfaces, foil handling, braid setup, reel transfers and selected peripherals.

SPECIALIST ITEMS Integrated from specialist manufacturers

Identify specialist instruments, test services and customer-supplied utilities separately. A machine list is not a complete acceptance package.

See HONGKAI process equipment in operation

These HONGKAI videos were selected for CAT6A / CAT7-relevant operations. They remain process references rather than proof that the exact source-schedule units, materials or finished-cable acceptance have been confirmed.

Request relevant evidence 5 HONGKAI process video references
  1. 01 REFERENCE 01 · TANDEM INSULATION

    CAT6A / CAT7 Tandem Insulation

    Category-specific tandem-insulation reference. Confirm the 60+35 configuration, insulation material and physical-foaming route separately. Watch on YouTube Opens in a new tab.
  2. 02 REFERENCE 02 · PAIR TWISTING

    High-Speed LAN Pair Twisting

    LAN pair-twisting process reference. Confirm the scheduled 500 back-twist arrangement and approved pair geometry separately. Watch on YouTube Opens in a new tab.
  3. 03 REFERENCE 03 · PAIR FOIL TAPING

    CAT6A / CAT7 Pair-to-Pair Taping

    A more relevant pair-foil process reference. Confirm the number of taping heads, foil route and complete core-assembly configuration separately. Watch on YouTube Opens in a new tab.
  4. 04 REFERENCE 04 · SHEATHING

    HK-80 Cable Sheathing Line

    Outer-sheath process reference. Confirm the scheduled 80 line and approved compound. Watch on YouTube Opens in a new tab.
  5. 05 REFERENCE 05 · COILING

    LAN Cable Coiling Machine

    LAN-cable coiling reference. Confirm that the actual machine is the scheduled 500 unit and matches the required coil and packing format. Watch on YouTube Opens in a new tab.

These five references do not cover or verify all eight equipment families. No confirmed video has been assigned to the cross separator, the source-schedule physical-foaming line or the 24-carrier metal braider. No video here establishes the new project's acceptance result, output or guaranteed cable performance. Reference 03 illustrates pair-to-pair taping but does not confirm the complete four-pair shielding path.

A useful project reference must match more than the cable category

For a CAT6A / CAT7 project, compare the actual insulation, pair-foil and overall-shield construction. A similar machine or category label alone is not a matching acceptance reference.

  • Cable construction

    Category, solid/foam insulation, separator, individual pair foil, overall shield and jacket are identified.

  • Equipment scope

    Match all eight scheduled equipment families, quantities, foil paths, tooling and included services.

  • Media approval

    Customer identity, country and project media are disclosed only with permission.

  • Documented result

    Category, test method, frequency range, limits, trial conditions and results are supported by project records.

The supplied schedule is headed 6E. It is an equipment-planning reference, not evidence of CAT6A / CAT7 compliance. Confirm the project drawing and acceptance basis separately.

Customer experience · CAT6 projects

These customer-approved comments describe existing CAT6 projects. They are retained as HONGKAI planning experience, not reviews or acceptance evidence for CAT6A / CAT7 equipment.

HONGKAI team with a customer group beside cable production equipment
CUSTOMER VISIT
CAT6 PROJECT
EXISTING CAT6 REVIEW

For our CAT6 project, HONGKAI explained how conductor insulation, pair-specific twisting and cabling settings relate to the agreed electrical test requirements. This made the proposed equipment scope easier to understand.

CUSTOMER Sumon Reza CAT6 project
HONGKAI representative with a customer team at a cable machinery site
CUSTOMER VISIT · INDONESIA
CAT6 PROJECT
EXISTING CAT6 REVIEW

The CAT6 planning discussion covered the workshop layout, utility interfaces and separator handling where required by the cable drawing. That gave our team a clearer basis for reviewing the proposed production route.

CUSTOMER Tariq Abdullah Indonesia
HONGKAI representatives with a customer group
CUSTOMER VISIT · BRAZIL
CAT6 PROJECT
EXISTING CAT6 REVIEW

We valued the clear distinction between a CAT6 U/UTP route and the additional overall foil and drain-wire handling for F/UTP. The proposal discussion also identified which testing and supply-scope details needed confirmation.

CUSTOMER Maria da Silva Brazil

Questions buyers ask before configuration

Need a project-specific answer? Send the cable specification and factory conditions below.

Does the equipment schedule confirm CAT6A / CAT7 compliance?

No. The supplied schedule is headed 6E. CAT6A / CAT7 suitability still requires an approved cable drawing, confirmed insulation and shielding paths, and a project-specific electrical acceptance plan.

Does a braiding machine make the route S/FTP?

Not by itself. The schedule includes taping and metal braiding, but four independent pair-foil paths are not yet confirmed. Check each pair wrap and the overall shield against the intended cable construction.

Is the physical-foam line specified for PE?

The supplied description names physically foamed FEP. Do not substitute PE or another compound without reviewing the material system, tooling and process conditions. Confirm the insulation route for each intended product.

Do all listed machines form one continuous line?

The schedule lists eight equipment families, including eight pair-twisting units, two cabling/taping units and ten braiding units. These quantities do not prove balanced output. Confirm batch routing, reel transfers, changeovers and capacity against the product mix.

Which information is needed before quotation?

Provide the intended category, cable drawing, conductor and insulation details, separator, individual pair-foil and overall-shield construction, jacket and fire requirements, target output, workshop utilities and acceptance tests.

Does a continuity test prove the cable category?

No. Continuity and identification are basic checks. Agree the CAT6A or CAT7 test standard, frequency range, limits, shielding checks and instrument capability before defining acceptance.

Who supplies the specialist equipment and tests?

The proposal should identify HONGKAI-manufactured modules, integrated specialist items and customer-supplied interfaces separately. Final test instruments, laboratory checks and responsibilities are agreed project by project.

Are the listed speeds guaranteed production output?

No. Design speed, core-wire speed and foaming speed describe different conditions. Usable output for each stage and the complete route must be confirmed against the materials, cable construction, configuration and acceptance conditions.

Share the cable information available today

Start with the intended CAT6A / CAT7 drawing, insulation material, pair-foil and overall-shield construction. Add your factory conditions and acceptance requirements so HONGKAI can review the equipment scope.

CURRENT PAGE SELECTION CAT6A / CAT7 project brief
Cable construction
To be confirmed
Project scenario
To be confirmed
Starting configuration
To be confirmed
Acceptance basis
To be confirmed

Topics for preliminary review

  • Insulation, separator and shielding inputs
  • Eight-family equipment and capacity review
  • Factory utilities and acceptance-test scope

This enquiry supports an initial technical discussion. It is not a quotation, performance guarantee, confirmed equipment list, final supply scope, delivery schedule or acceptance commitment.

LAN Cable Equipment Project Enquiry
Drag & Drop Files, Choose Files to Upload

Ask for quote

we will reply you within 24 hours!!!