
هل تواجه صعوبة في التعامل مع تعقيدات تصنيع القلب الليفي؟ يؤدي ضعف مراقبة الجودة إلى فقدان الإشارة وفشل الإنتاج.
تبدأ عملية إنتاج الألياف الضوئية باستخدام سبيكة زجاجية (preform)، تليها عمليات التسخين، السحب، التحكم في القطر، والتطليع الواقي. تحتوي الألياف الزجاجية المسحوبة على كل من القلب والغلاف؛ فهي ليست قلباً معزولاً. تأكد من مسار السبيكة، وإعدادات الفرن، ومواصفات الألياف النهائية للعملية المختارة.
When assessing a fiber core manufacturing project, distinguish glass preform fabrication and fiber drawing from downstream cable production. Use this guide to identify the process stages, equipment interfaces and evidence to request from suppliers. For a HONGKAI Cable Machinery enquiry, confirm the proposed equipment scope, responsible manufacturer and acceptance requirements in the project documents.
ما هي المواد التي تحتاجها لإنتاج الألياف الأساسية؟
تُعد تركيب المواد الخام والتحكم في التلوث جزءاً من جودة الألياف، لكنها ليست العوامل الوحيدة. قيّم سجلات المواد جنباً إلى جنب مع فحص التشكيلات الأولية واختبارات الألياف النهائية؛ ولا تشخص الفقد البصري أو كسور الألياف بناءً على درجة النقاء الاسمية فقط.
Define the intended fiber and preform route before specifying chemical inputs. A chloride-based MCVD process uses volatile glass-forming precursors, but material grades, dopants, gases and thermal settings must match the qualified process. Buying finished preforms is a different supply scope from manufacturing them.
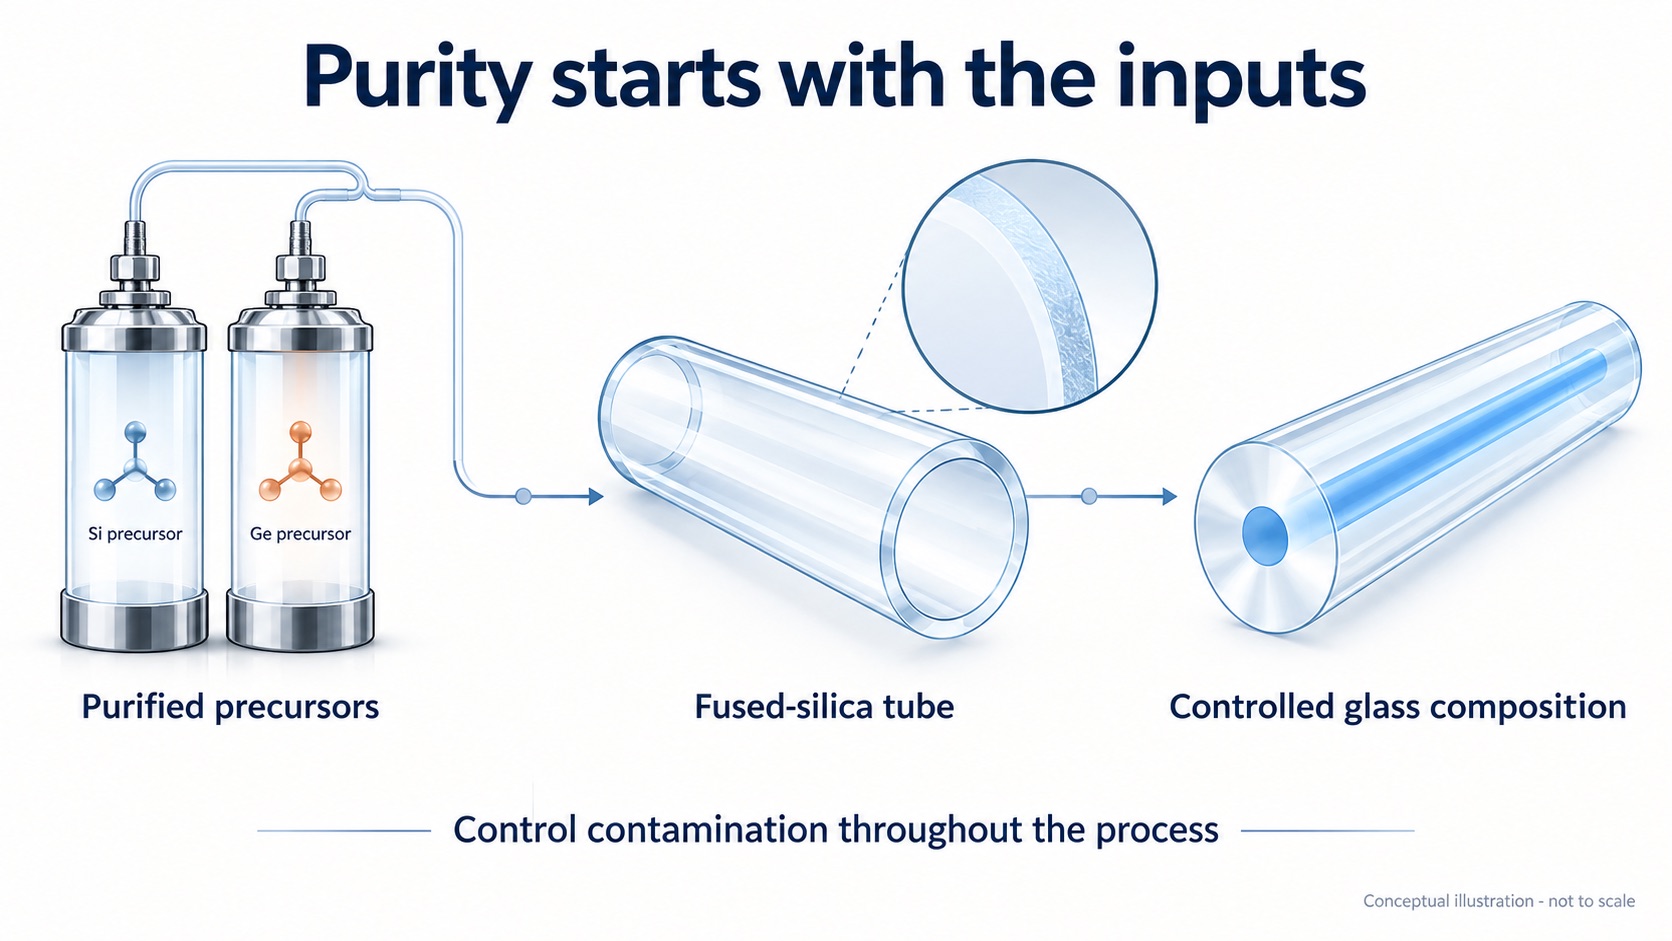
رسم توضيحي مفاهيمي لمدخلات المواد والتحكم في التلوث أثناء تحضير البلورة الأولية؛ وليس صورة مختبرية.
Raw-material selection and contamination control belong in the project’s quality plan. Request material specifications and batch records from the proposed producer, and confirm how nonconforming batches are handled. نظرة عامة على إنتاج هيرايوس للألياف البصرية يوضح أدوار تركيب المادة، والهندسة، وملف معامل الانكسار. لا تُعرِّف نسبة النقاء وحدها أداء الألياف النهائي.
المكونات الكيميائية الأساسية
ال وصف MCVD من جامعة لايبنتس هانوفر identifies SiCl4, GeCl4 and POCl3 as examples of volatile glass-forming precursors. This is not a mandatory ingredient list for every fiber. For each selected chemical, request the supplier’s grade specification, batch certificate and relevant trace-impurity results; the process owner must approve its suitability.
Germanium doping can raise the refractive index of silica, but the finished fiber must be defined by its complete core-and-cladding design. Do not infer numerical aperture or other optical performance from a germanium concentration alone. Confirm the intended refractive-index profile, dopant formulation and applicable measurements with the preform producer.
عملية التفاعل الكيميائي
In the MCVD route described by Leibniz University Hannover, precursor vapors pass through a fused-silica tube and an external traversing burner initiates glass formation. Particles deposit on the tube’s inner wall. Deposition, consolidation and tube collapse are distinct stages; one generic reaction-temperature range is not an operating specification for all of them.
Require the process owner to define and qualify the temperature and gas-delivery settings for each stage. The production record should identify the recipe version, measured variables, permitted deviations and response to an excursion. Do not adopt an unsourced temperature-change threshold or flow-stability percentage as proof of complete reaction or acceptable fiber.
متطلبات النقاء والاختبار
Define impurity limits for the specific input material and intended fiber, not by comparison with another industry. Heraeus’ overview distinguishes hydroxyl-content requirements for UV and infrared transmission, illustrating why application matters. For moisture, metals and other specified impurities, identify the material being tested, concentration units, analytical method and reporting limit. Do not interchange a precursor-gas specification with a finished-glass measurement.
Request the producer’s incoming-material inspection plan, batch certificates and laboratory reports. Ask which analytical methods are used, which contaminants are assessed and how each result is compared with the agreed material specification. Confirm the responsible laboratory and traceability arrangements rather than assuming that the equipment supplier performs these tests.
استخدم هذه المصفوفة لتحديد وثائق قبول المواد الواردة. إنها ليست مواصفة عالمية لنقاوة المواد الكيميائية أو إجراء اختبار مختبري.
| إدخال للتأهيل | المواصفات للحصول عليها | دليل الدفعة أو التوريد | Acceptance decision |
|---|---|---|---|
| SiCl4، إذا تم استخدامه | الدرجة المؤهلة وحدود الشوائب المحددة مع الوحدات | شهادة الدفعة، والنتائج التحليلية ذات الصلة وحدود الإبلاغ | يُوافق مالك العملية على المادة المخصصة للوصفة المطلوبة |
| GeCl4 أو مادة أولية مُضافة أخرى، إذا تم استخدامها | الكيمياء المختارة، والدرجة وحدود الشوائب لتصميم الألياف | نتائج الدُفعات القابلة للتتبع باستخدام طرق مناسبة لذلك المادة | قارن مع مواصفات مادة المُشوِّب المعتمدة |
| O2, if used | درجة الغاز وحدود الملوثات المطلوبة من قبل العملية | تزويد شهادة التوريد وفحوصات نقطة الاستخدام المتفق عليها | تحقق من ظروف توصيل الغاز المحددة |
| غازات الحمل أو الغازات المستخدمة في المعالجة، إذا استُخدمت | متطلبات هوية الغاز ونقاوته والتوصيل للمسار الفعلي | سجلات المورّد وفحوصات حالة الخط المتفق عليها | الموافقة وفقًا لمواصفات مرافق العمليات |
اعتبارات التخزين والمناولة
Before specifying chemical storage, request the current safety data sheets and the chemical supplier’s storage and compatibility requirements. Have the proposed facility design reviewed by qualified personnel. Container materials, atmosphere controls and environmental limits must be established for the actual chemicals and process, not inferred from a generic article.
Require documented procedures for chemical transfer, contamination control, personnel protection and emergency response. Confirm tubing and fitting compatibility, any purge requirements and the applicable training with the responsible process and safety specialists. This overview is not an operating procedure for chemical handling.
Include the required material-handling facilities, inspection work and maintenance in the project scope and cost comparison. Ask for the proposed producer’s contamination-control records, and confirm which safeguards and records are included before comparing quotations.
كيف تصنع قالب الزجاج؟
تؤثر جودة المسبوك بشكل مباشر على خصائص الألياف. يؤدي الترسيب غير المنتظم إلى تباين في القطر وفقدان بصري على طول الألياف.
MCVD deposits glass on the inside wall of a silica tube. OVD builds a porous soot preform around the outside of a target rod before consolidation. These are different fabrication routes; preform dimensions depend on the selected process and equipment.
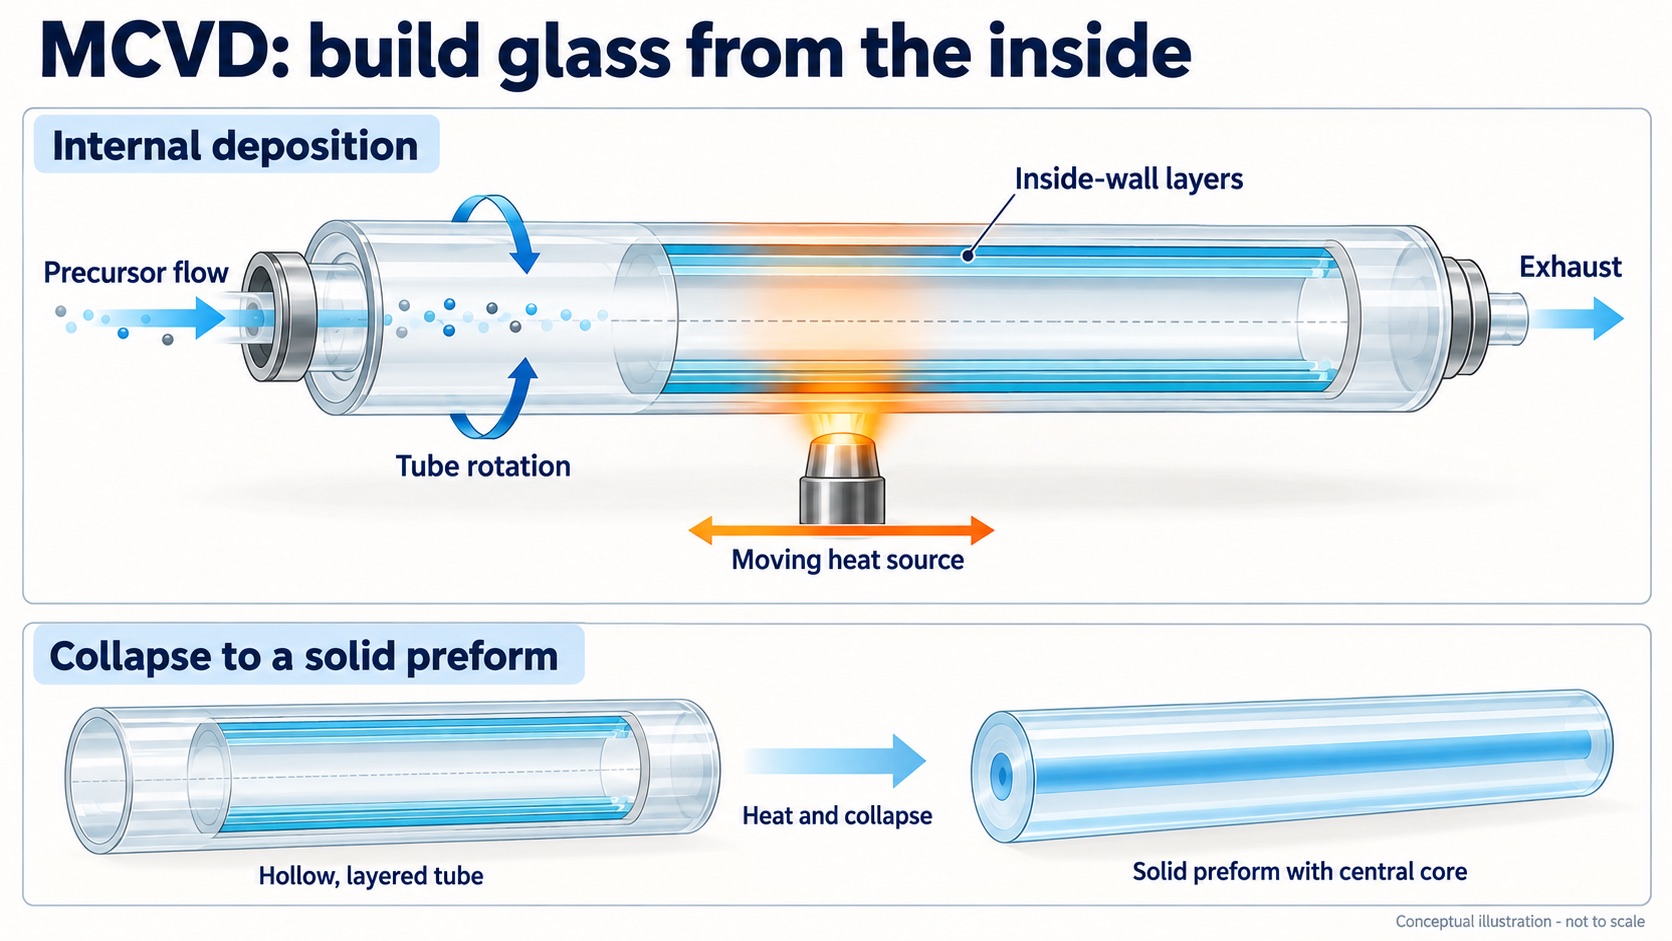
رسم توضيحي مفاهيمي لتقنية MCVD: يتم ترسيب الزجاج داخل الأنبوب قبل ضغطه إلى قالب أولي صلب. غير مُرسَم وفقًا للنسبة.
For a fiber core manufacturing project, confirm whether preforms will be purchased or fabricated as part of the proposed scope. Request the preform specification, inspection records and compatibility requirements for the drawing equipment. Identify the party responsible for preform production separately from the equipment supplier.
عملية الترسيب الكيميائي للبخار المعدل (MCVD)
In the عملية MCVD الموصوفة من قبل جامعة لايبنتس هانوفر, precursor gases flow through a fused-silica tube while an external burner travels along it. Glass particles form and deposit on the tube’s inner wall. The gas composition and deposition conditions control the refractive-index profile; tube dimensions must match the specific process and equipment.
For the proposed MCVD lathe and traversing burner, obtain the qualified tube-size range, rotation and traverse settings, alignment requirements and thermal-control method. Identify whether a reported temperature refers to the flame, tube surface or another target. Treat rotation speed and temperature as equipment- and recipe-specific values rather than universal MCVD settings.
Review the gas-delivery sequence and control arrangement for the proposed MCVD process. Require calibrated flow measurement, a documented deposition schedule and traceable process records. The number of passes, deposited-layer dimensions and permitted flow variation must come from the qualified preform design and demonstrated process, not an assumed standard cycle.
The deposition process creates "soot" – submicron glass particles that form in the hot zone and deposit on the inner wall of the tube. The high temperature consolidates these particles into dense, transparent glass as the burner passes over the deposited soot. The consolidation temperature must be carefully controlled to prevent bubble formation while ensuring complete densification.
عملية الترسيب البخاري الخارجي (OVD)
In شرح كورنينغ لترسيب البخار الخارجي, تتراكم جسيمات الزجاج الدقيقة، والمعروفة باسم السخام، حول الجزء الخارجي لقضيب الهدف أو "قضيب الطُعم". وعلى عكس عملية MCVD، فإن هذا الترسيب لا يحدث على الجدار الداخلي لأنبوب الركيزة.
Successive soot layers build outward around the target. The deposition equipment and dopant delivery must follow the intended preform design. This is an external buildup of soot, not deposition within a hollow tube.
Preform size and production output are equipment-specific. Do not use one diameter or length as a universal OVD capability; confirm the qualified preform range with the process-equipment supplier.
في المسار الذي وصفته شركة كورنينغ، تتم إزالة قضيب الطُعم قبل التوحيد. أثناء ال مرحلة توحيد OVD, يحوّل الحرارة الجسمَ السُّودي المسامي إلى زجاج كثيف وشفاف. يجب أن تتبع ظروف التوحيد العملية المؤهلة بدلاً من وصفة حرارية عامة.
مراقبة الجودة أثناء تصنيع القوالب المسبقة
For thermal monitoring during preform fabrication, specify the actual measurement target and the instrument suitable for it. Ask the supplier to state calibration, measurement uncertainty and relevant operating limitations. A non-contact temperature reading should not be treated automatically as an accurate flame-temperature or glass-temperature measurement.
Ask the preform producer for refractive-index profile measurements and the stated test method. The report should identify the measured preform, instrument, calibration status and acceptance criteria. Agree how out-of-specification results are handled before the preform is released for drawing.
Include preform diameter, concentricity, straightness and roundness in the agreed dimensional inspection plan. Require the supplier to state the measurement method, units and acceptance tolerances for the specified preform and drawing equipment. Do not adopt an unsourced percentage as a universal limit.
Compare MCVD and OVD proposals against the same intended fiber design and supply scope. Route names alone do not establish fixed core diameters, numerical apertures or attenuation limits. Keep preform inspection separate from acceptance of the fiber drawn from it.
| البند للمقارنة | أدلة اقتراح MCVD | أدلّة مقترح OVD | Acceptance boundary |
|---|---|---|---|
| مسار الترسيب والمرحلة الموردة | تحديد أنبوب الركيزة، الترسيب الداخلي ومرحلة البريفورم المورَّدة | تحديد ترسب السخام الخارجي، والتجميع، ومرحلة التشكيلة المورَّدة | قارن مراحل التوريد المكافئة، وليس تسميات المسارات وحدها |
| Preform geometry | نتائج الرسم والفحص للشكل الأولي المقترح | نتائج الرسم والفحص للشكل الأولي المقترح | اذكر ما إذا كانت كل بُعد يشير إلى الشكل الأولي أو الألياف المسحوبة، مع الوحدات |
| مقطع معامل الانكسار وتصميم الألياف | الملف الشخصي المقاس ومواصفات الألياف المستهدفة | الملف الشخصي المقاس ومواصفات الألياف المستهدفة | يجب الاتفاق على المقطع العرضي وأي اختبار مناسب للفتحة العددية بشكل منفصل |
| التمركز، الاستقامة والاستدارة | طريقة الفحص، النتائج المقاسة والتسامحات المقترحة | طريقة الفحص، النتائج المقاسة والتسامحات المقترحة | تطبيق رسمة التشكيل المسبق المعتمدة وخطة الفحص |
| أداء الألياف البصرية النهائية | نتائج قابلة للتتبع من الألياف المسحوبة من البريفورم المقترح | نتائج قابلة للتتبع من الألياف المسحوبة من البريفورم المقترح | استخدم مواصفات الألياف المختارة وظروف الاختبار المتفق عليها، وليس حدًا عامًا لـ MCVD/OVD |
تحسين العمليات واستكشاف الأخطاء وإصلاحها
Require a documented trial plan before changing preform-fabrication parameters. Identify the variables, permitted operating boundaries, measurements and approval responsibilities with the process owner. Keep trial results traceable to the material batch and equipment settings, and record the process owner’s approval.
For a suspected preform defect, first identify the measured feature: interface condition, refractive-index profile or geometry. Compare inspection results with the approved preform design and the corresponding material, deposition and equipment records. A defect name alone does not establish whether contamination, thermal conditions, gas delivery or alignment caused it. Ask the process owner to document the evidence for the proposed cause before changing the recipe.
Request the equipment manufacturer’s preventive-maintenance schedule and calibration requirements. Confirm which burner components, flow controllers and alignment checks are included, who performs each task and what records are required. Agree the maintenance scope before equipment acceptance.
Preform acceptance is one checkpoint, not a guarantee of trouble-free drawing. Link each preform’s inspection record to the drawing run and finished-fiber results so a defect can be investigated across stages. Release the fiber only against the agreed geometry, optical and mechanical requirements.
ما هي المعدات الأساسية لرسم الألياف؟
يؤدي اختيار المعدات الخاطئة إلى فشل الإنتاج. كما أن أنظمة السحب غير الملائمة تُسبب تكسر الألياف، واختلافات في القطر، وعيوبًا في الطلاء، مما يجعل المنتج غير صالح للاستخدام.
Specify the drawing system as a complete process: preform feed, furnace, cooling, diameter measurement, coating, curing and take-up. Require the supplier to demonstrate the agreed fiber dimensions and quality at the proposed production speed; a speed figure alone is not an acceptance criterion.
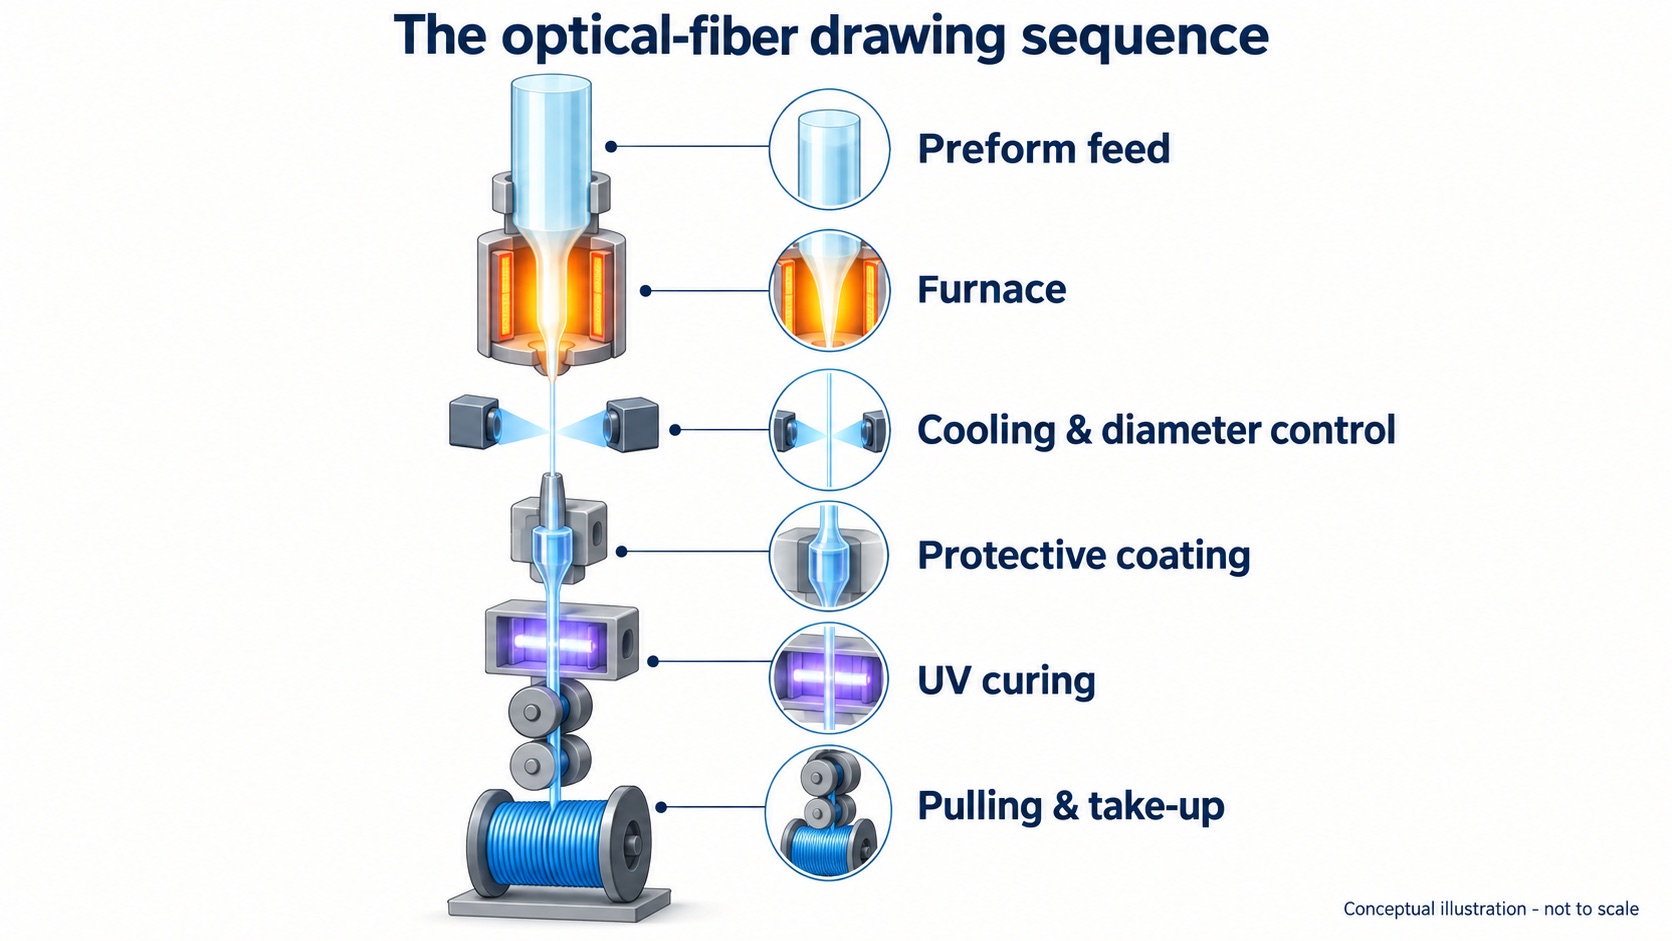
تسلسل مرحلة الرسم المفاهيمي، وليس رسمًا لآلة مورَّدة محددة. غير مرسوم وفقًا للقياس.
Coordinate the interfaces between the preform, drawing equipment and coating system before accepting a line proposal. Record the target fiber type, glass-cladding diameter, coated-fiber outer diameter and test conditions so each supplier works to the same product definition.
رسم هيكل البرج وتصميمه
When reviewing a برج سحب الألياف, request the supplier’s layout, structural requirements and vibration-control provisions for the proposed configuration. Confirm the required building height, foundations, service access and utility interfaces from the actual equipment drawings rather than assuming a standard tower size.
يضم البرج مناطق متعددة، لكل منها وظيفة محددة في عملية السحب. يحتوي القسم العلوي على آلية تغذية القالب المسبق والفرن. يوفر القسم الأوسط مساحة لتبريد الألياف وقياس القطر. أما القسم السفلي، فيضم نظام تطبيق الطلاء، وأفران المعالجة، ومعدات السحب.
Ask the drawing-equipment and coating suppliers to specify the required cleanliness, temperature, humidity and ventilation conditions. Record operating and shutdown requirements in the utility schedule, together with monitoring methods and acceptance limits. Assign responsibility for establishing and maintaining these conditions.
أنظمة الفرن عالية الحرارة
Confirm the furnace heating technology, usable hot zone, preform-size range and qualified operating window with the equipment manufacturer. Furnace dimensions and maximum temperature must come from the proposed equipment specification, not a generic production-line example.
Request the furnace supplier’s temperature-measurement and control specification, including sensor type, calibration, measurement uncertainty and demonstrated control performance. Distinguish a stated controller resolution from verified furnace stability, and agree the acceptance test for the supplied system.
Confirm furnace-gas requirements with the furnace manufacturer and responsible process engineer. The utility specification should identify gas type, quality, flow requirements, monitoring and safety provisions for the actual system. Do not use a generic oxygen limit or gas selection as an approved operating recipe.
For the preform-feed system, request the supported preform dimensions and mass, feed range, positioning performance and coordination with draw control. Agree a test using the intended preform rather than assuming a universal positioning tolerance.
قياس القطر والتحكم فيه
Specify what each gauge measures: bare-glass outer diameter, coated-fiber outer diameter or another defined feature. Request the instrument’s measurement range, accuracy, repeatability, sampling rate and calibration requirements. Do not treat resolution, response time and achieved production tolerance as interchangeable specifications.
Draw speed is one control variable used to regulate bare-glass diameter, but it interacts with preform feed, thermal conditions and tension. Confirm which variables the proposed controller actually adjusts, where the diameter is measured and how transport delay is handled. Require a recorded trial showing diameter and tension together during steady running and approved speed changes; a simple ‘speed up when thick’ rule is not a complete control specification.
يجب التعامل مع التحكم التنبؤي والقائم على التعلّم باعتباره وظائف مقترحة محددة، وليس ميزات قياسية في كل خط رسم. على سبيل المثال، ورقة البحث التحكم الديناميكي في عملية تصنيع الألياف باستخدام التعلم المعزز العميق reports tests on a compact fiber-drawing system. It does not establish deployment or performance on the production line being quoted. Request the actual control architecture, operating limits and acceptance demonstration for any such claim.
| معامل | عرّف في الاقتراح | أساس القبول | الأدلة المطلوب طلبها |
|---|---|---|---|
| Furnace operation | تكنولوجيا التسخين، ومنطقة الحرارة القابلة للاستخدام، ونافذة التشغيل | الإعدادات المؤهلة للشكل الأولي المحدد | مواصفات المعدات وظروف التجربة المسجلة |
| قطر الغلاف الزجاجي | قطر الزجاج الخارجي غير المغلف، وهو يختلف عن قطر القلب | الهدف والتسامح في مواصفات الألياف المحددة | بيانات المقياس المعاير وطريقة الفحص المتفق عليها |
| سرعة الرسم | سرعة الإنتاج المتفق عليها للألياف المحددة | الجودة المُثبتة عند تلك السرعة | سجل تجريبي يربط السرعة بالهندسة والنتائج البصرية |
| قطر الألياف المغلفة الخارجي | القطر فوق الطلاء المعالج، وليس السُمك الشعاعي للطلاء | الهدف والتسامح للتصميم المختار للطلاء | نتائج القطر والتمركز من الاختبار المتفق عليه |
أنظمة تطبيق الطلاء
يُطبّق نظام الطلاء طبقات بوليمر واقية على الألياف الزجاجية العارية فور تشكيلها. يجب تطبيق الطلاء بشكل مركزي وموحد لمنع خسائر الانحناء الدقيق وتوفير حماية ميكانيكية. تستخدم معظم الأنظمة قوالب ضغط تُجبر مادة الطلاء السائلة على الدوران حول الألياف.
The primary coating is the polymer layer next to the glass. Confirm its material, cured outer diameter and acceptance requirements in the qualified coating design. Do not assume a fixed radial thickness for every optical-fiber product.
The secondary coating surrounds the primary layer. Distinguish its outer diameter from the thickness of either layer. For concentric circular layers, total radial coating thickness = (coated-fiber outer diameter – glass-cladding diameter) / 2. This relation alone does not determine how the thickness is divided between primary and secondary coatings.
لمثال محدد للمنتج،, Corning’s SMF-28 Ultra product sheet, July 2025, page 2 lists a glass-cladding diameter of 125.0 ± 0.7 μm and coated diameters of 242 ± 5 μm or 200 ± 5 μm, depending on the option. Using nominal diameters gives combined radial coating thicknesses of 58.5 μm and 37.5 μm respectively. These are calculated examples for that product, not universal coating recipes or HONGKAI equipment guarantees.
Request the proposed coating-concentricity measurement method and die-alignment procedure, with acceptance limits tied to the specified fiber and coating system. Keep geometry checks and optical-performance tests separate: a concentricity result alone does not establish the fiber’s polarization-mode-dispersion performance.
أنظمة المعالجة بالأشعة فوق البنفسجية
تُحوّل أنظمة المعالجة بالأشعة فوق البنفسجية طلاءات الأكريلات السائلة إلى طبقات واقية صلبة. يجب أن تكون عملية المعالجة كاملة وموحدة لضمان خصائص الطلاء المناسبة. قد يؤدي عدم اكتمال المعالجة إلى أسطح لزجة وخصائص ميكانيكية رديئة.
لا يقتصر علاج طلاء الألياف على تقنية مصباح واحدة. مذكرة تطبيق علاج الألياف بالأشعة فوق البنفسجية من إكسليتاس باستخدام الصمام الثنائي الباعث للضوء (UV-LED) describes conventional arc/microwave lamp systems and UV LED systems, and stresses testing the coating with the selected light source. Ask the coating and equipment suppliers to qualify the spectral match, exposure, optical arrangement and thermal conditions at the proposed line speed; lamp layout alone does not prove uniform cure.
If the proposed curing system uses nitrogen inerting, obtain the required gas specification, chamber conditions, monitoring and alarm limits from the coating and curing-equipment suppliers. Verify the cured coating against an agreed test method. Nitrogen supply alone is not evidence that the coating has reached its required cure state.
أنظمة التحكم في التوتر والرفع
Tension control throughout the drawing process is essential for consistent fiber properties. Excessive tension can cause fiber breaks or diameter variations, while insufficient tension can lead to loose winding and handling problems. Agree the drawing-tension range, force units, measurement method and acceptance conditions for the actual fiber and drawing system.
For the capstan system, request the drive-control specification, fiber-contact surface details and maintenance requirements. Ask the supplier to demonstrate the proposed speed-control performance and fiber-handling results under agreed test conditions rather than relying on an unsupported accuracy figure.
Take-up systems wind the finished fiber onto spools for storage and shipping. The winding pattern must prevent fiber damage while allowing easy unwinding for subsequent processing. Confirm the traverse mechanism, winding pattern and take-up tension requirements with the supplier, then verify the result using the agreed spool and fiber specification.
If the take-up uses a dancer, confirm its loading method, usable travel, position feedback and connection to reel-speed control. Verify winding tension during acceleration, steady running and spool build-up with the intended fiber and reel. A dancer’s presence does not guarantee constant tension, and take-up tension must not be confused with the tension measured in the hot drawing zone.
كيف يمكنك التحكم بجودة الألياف أثناء الإنتاج؟
مراقبة الجودة تمنع عيوب الإنتاج المكلفة. فبدون المراقبة المناسبة، قد تفشل عمليات الإنتاج بأكملها في تلبية متطلبات المواصفات، مما يؤدي إلى خسائر كبيرة في المواد والوقت.
Use a quality plan that separates inline process measurements from optical and mechanical acceptance tests. Define each measured feature, test method, inspection frequency and acceptance limit; inline diameter feedback alone does not verify every finished-fiber requirement.
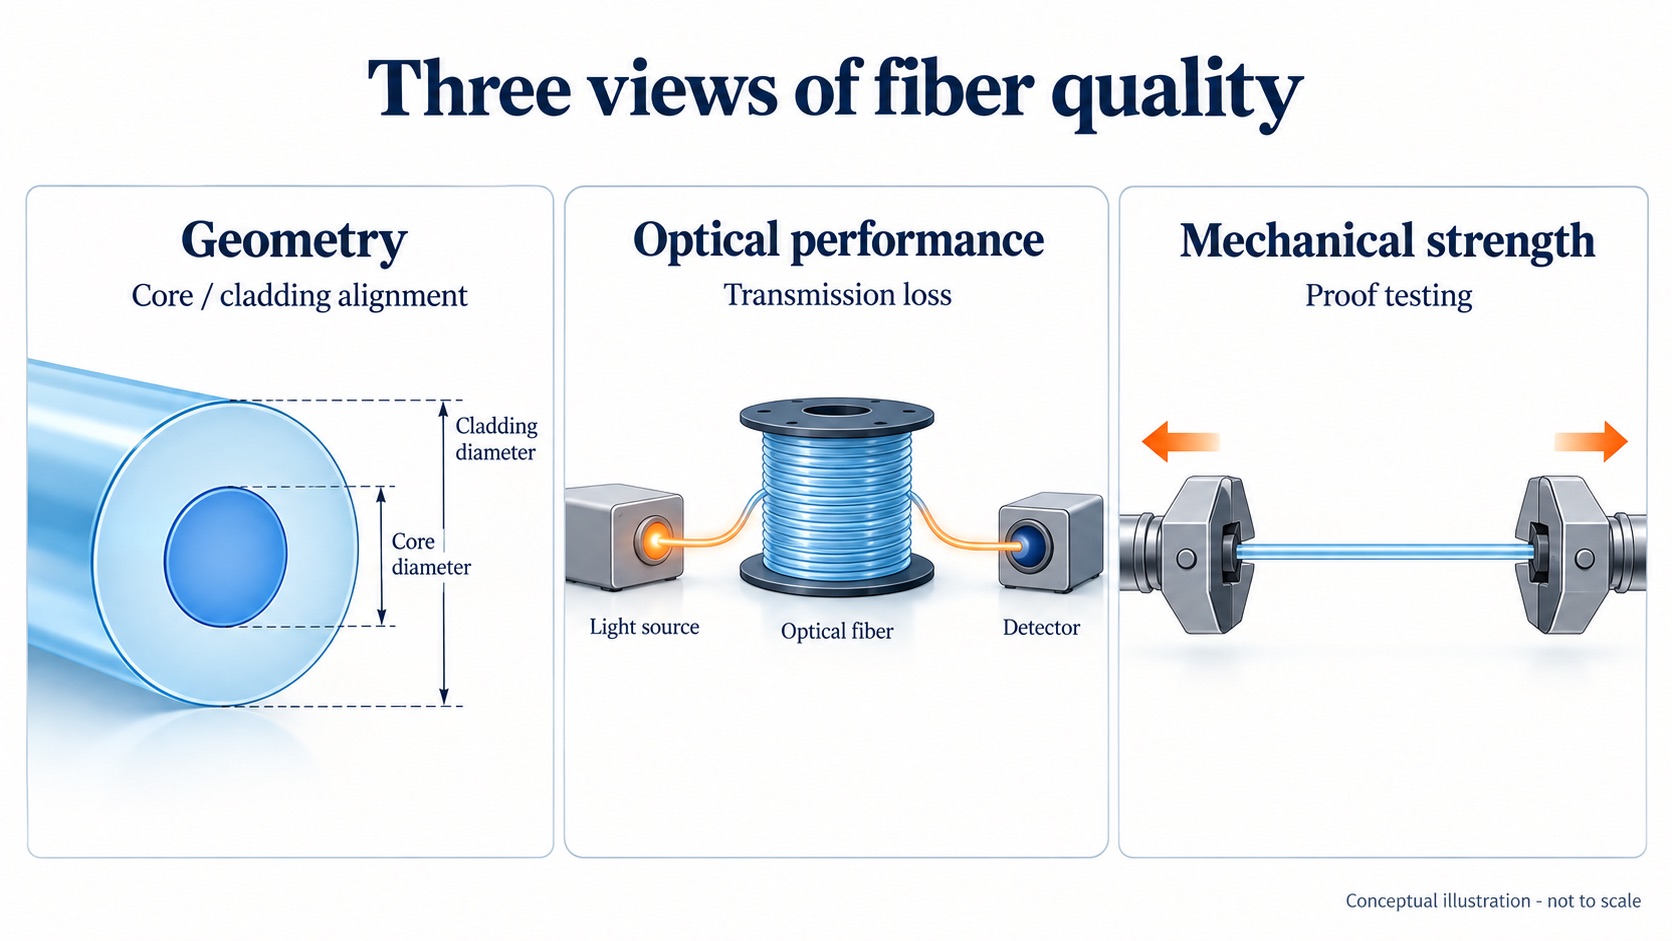
رسم توضيحي مفاهيمي للهندسة والفحوصات البصرية والميكانيكية؛ لا تظهر نتائج قياسات فعلية.
Define the fiber-production quality plan before accepting the equipment. Identify the measurements, inspection frequency, acceptance criteria and responsibility for nonconforming material at each stage. Request sample records from the proposed producer and agree which checks are included in the supplied scope.
مراقبة العمليات في الوقت الفعلي
For each inline measurement, record the sensor principle, accuracy, sampling rate, filtering and position on the line. Ask the supplier to demonstrate which defects the complete measurement-and-control system can detect at the proposed draw speed. Do not infer a minimum detectable defect length or closed-loop response from the gauge resolution alone.
For coating inspection, ask whether the proposed instrument reports coated outer diameter, concentricity or individual-layer geometry. An outer-diameter reading alone does not establish the separate primary and secondary layer thicknesses. Document which features are measured, the calibration method and how the results are checked against the selected coating design.
لا تفترض أن كل قياس لقوة شد الرسم يستخدم خلية تحميل. وصف SIKORA لقياس شد الألياف الضوئية discusses vibration-based measurement and a birefringence-based optical method. Confirm the proposed instrument, measurement location, units and validation procedure. Define separately whether its signal is displayed, logged, used for an alarm or connected to an automatic control loop; measurement alone does not prove automatic break prevention.
List the thermal and environmental measurements actually included in the proposed line, such as fiber temperature before coating and conditions in the coating or curing area. Identify each measurement target, sensor, logging interval and alarm boundary. Verify any thermal-imaging or contamination-monitoring function explicitly rather than assuming it is supplied with the tower.
اختبار الخصائص البصرية
اختر طريقة اختبار التوهين المناسبة للألياف والتقرير المطلوب. الـ IEC 60793-1-40:2024 attenuation-method overview lists cut-back, insertion-loss and backscattering methods, as well as spectral modelling with a narrower scope. Record the selected method, test wavelengths, launch conditions, sample identification and acceptance limits; do not assume every production test uses cut-back.
للبصريات متعددة الأنماط، عرّف معيار عرض النطاق الترددي المطلوب وشرط الإطلاق. IEC 60793-1-41:2024 distinguishes time-domain, frequency-domain and DMD-derived overfilled-launch bandwidth methods. IEC 60793-1-49:2018 describes DMD characterization of graded-index multimode fiber for bandwidth assessment under different launch conditions. Do not describe a DMD report as a direct refractive-index-profile measurement. Ask the laboratory to identify the fiber category, wavelength, method and reported bandwidth metric.
ميّز الفتحة العددية المقاسة عن القيمة المحسوبة باستخدام معاملات الانكسار. الـ IEC 60793-1-43:2015 overview covers specified multimode-fiber categories and distinguishes far-field numerical aperture from theoretical numerical aperture. Ask the laboratory to state the applicable fiber category, sample length, measurement threshold and uncertainty. Do not use a numerical-aperture result as a substitute for a required single-mode cutoff-wavelength test.
بالنسبة للألياف ذات الوضع الواحد، حدد طريقة اختبار قطر مجال الوضع (MFD) وطول الموجة المبلغ عنها معًا. IEC 60793-1-45:2024 addresses MFD measurement. Compare results with the selected fiber specification at the same stated wavelength; do not treat an MFD value without its wavelength as a complete acceptance requirement.
اختبار الخواص الميكانيكية
Proof testing applies a specified tensile stress to screen fiber for weak sections. As one documented example, section 1.4 of مواصفات ألياف Corning PGSF001 يحدد الحد الأدنى لـ 100 kpsi (approximately 0.69 GPa) for the fibers covered by that document. Here, 100 kpsi means 100,000 psi. Use the applicable fiber specification and test procedure for the product being manufactured.
Coating adhesion testing verifies that the polymer coatings bond properly to the glass surface and to each other. Poor adhesion can lead to coating delamination during handling or environmental exposure. Request the applicable coating-adhesion and stripping test procedures, reported results and acceptance criteria from the fiber producer.
يُقيّم اختبار الانحناء مقاومة الألياف لخسائر الانحناء الكلي والجزئي. تُغلّف اختبارات الانحناء الكلي الألياف حول قضبان بأقطار مختلفة لمحاكاة ظروف التركيب. وتُطبّق اختبارات الانحناء الجزئي ضغطًا جانبيًا مُتحكّمًا به لمحاكاة آثار تصنيع الكابلات والضغوط البيئية.
تُعرِّض الاختبارات البيئية عينات الألياف لدورات الحرارة والرطوبة والبيئات الكيميائية التي قد تواجهها أثناء التشغيل. تساعد هذه الاختبارات على التنبؤ بالموثوقية على المدى الطويل وتحديد أنماط الأعطال المحتملة قبل حدوثها في الموقع.
Use the following planning matrix to agree the product-specific quality plan. A measurement standard defines how a test is performed; it is not, by itself, a universal product limit or a sampling plan. Adapt the wavelength rows to the selected fiber rather than applying them to every fiber type.
| Test parameter | طريقة التحديد | التغطية أو أخذ العينات حسب الاتفاق | أساس القبول |
|---|---|---|---|
| Attenuation at 1310 nm, if specified | Applicable method under IEC 60793-1-40:2024 | مُعرَّف في خطة جودة المنتج | Maximum loss for the selected fiber at this wavelength |
| Attenuation at 1550 nm, if specified | Applicable method under IEC 60793-1-40:2024 | مُعرَّف في خطة جودة المنتج | Maximum loss for the selected fiber at this wavelength |
| MFD للألياف أحادية النمط عند الطول الموجي المذكور | Applicable method under IEC 60793-1-45:2024 | مُعرَّف في خطة جودة المنتج | القيمة الاسمية والتحمل عند نفس الطول الموجي ذلك |
| اختبار الإثبات | IEC 60793-1-30:2010 fibre proof-test procedure | الطول المطلوب اختباره وسجلات البكرة القابلة للتتبع | مستوى الإجهاد وقواعد القبول من مواصفات الألياف المحددة |
| قطر الألياف المغلفة الخارجي | طريقة اختبار الأبعاد المتفق عليها | مُعرَّف في خطة الجودة | الهدف والتسامح من مواصفات الألياف/الطلاء المحددة |
التحكم الإحصائي في العمليات
Statistical process control (SPC) can help identify changes in recorded process measurements. توجيهات NIST حول مخطط التحكم explains that both points outside control limits and non-random patterns can warrant investigation. Control limits describe process behavior; they are not the product’s specification limits. A stable process can still produce nonconforming fiber. For the proposed quality system, identify the measured feature, chart type, sampling method, investigation rules and responsible person. Confirm whether alerts are actually implemented; a chart alone does not prevent defects or release a spool for shipment.
قبل تفسير Cp أو Cpk، تأكد من أن العملية مستقرة وأن البيانات وطريقة الحساب مناسبة. NIST’s process-capability overview compares stable-process variation with specification limits and states the normal-distribution assumption of the conventional indices. Cp compares specification width with process spread; Cpk also accounts for an off-center process mean. Ask for the underlying measurements, units, sampling period, specification limits and statistical assumptions, not just an index on a dashboard. Agree any required capability criterion for the project; do not substitute an unsourced universal threshold for the fiber’s acceptance tests.
Design of experiments (DOE) techniques help optimize process parameters and understand the relationships between different variables. For any proposed optimization trial, agree the factors, response measurements and permitted operating boundaries with the process owner, and require a traceable report of the results.
Correlation analysis helps identify relationships between different measurements that might not be obvious. Treat a measured correlation as a finding to investigate, not proof of a causal relationship or a guaranteed process improvement.
أنظمة الجودة الآلية
For an automated quality-control proposal, require a list of measured inputs, controlled outputs, alarm actions and operator responsibilities. Ask the supplier to demonstrate each promised feedback or predictive function on the proposed system. Do not assume that machine-learning prediction or automatic defect prevention is included in a standard drawing line.
Specify which process and test data will actually be recorded, with timestamps, length or spool references, retention and export requirements. Check a sample production record before acceptance; an automation interface does not establish that every quality parameter is captured or traceable.
Ask the supplier to demonstrate how an out-of-specification segment is identified, located, segregated and documented. State whether handling requires stopping, cutting, transfer or later rewinding, and define the restart and retest procedure. Do not assume defective fiber can be removed while drawing continues without interruption.
If ERP or other factory-system integration is required, define the data fields, spool identifiers, interfaces, access rights and responsibility for failed transfers. Test a sample record from measurement through export and retrieval before acceptance. An available interface does not by itself establish end-to-end traceability or regulatory compliance.
ما هي مشاكل التصنيع الشائعة وحلولها؟
قد تؤدي مشاكل الإنتاج إلى توقف خطوط تصنيع كاملة. وتؤدي المشاكل غير المُحَلّة إلى تلف المعدات، وهدر المواد، وعدم الوفاء بالتزامات التسليم، مما يُضرّ بالعلاقات مع العملاء.
تتطلب الانقطاعات في الألياف، والاختلافات في القطر، وعيوب الطلاء إجراءات استكشاف أخطاء منهجية وبروتوكولات صيانة وقائية للحفاظ على جودة إنتاج متسقة.
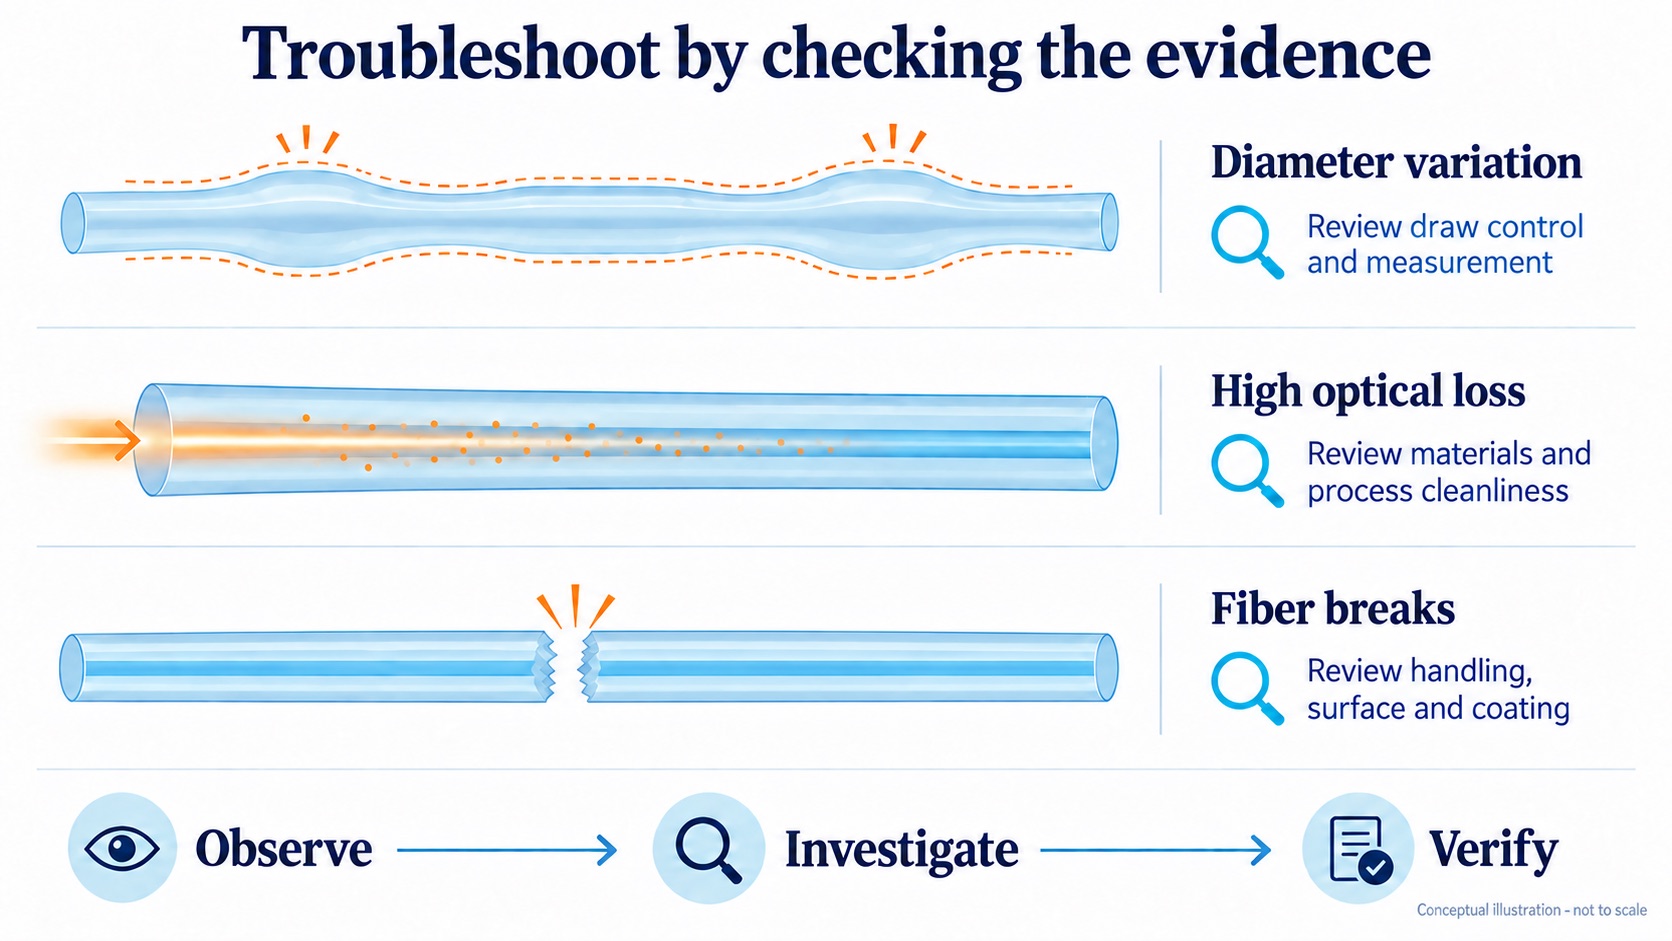
رسم توضيحي مفاهيمي لاستكشاف الأخطاء. الفحوصات المذكورة هي مطالبات تحقيق، وليست أسبابًا مؤكدة أو إصلاحات مضمونة.
Use production records, alarms, inspection results and supplier procedures to investigate fiber-manufacturing problems. Establish the observed symptom and operating conditions before proposing a cause. Follow the applicable manufacturer’s safety and maintenance instructions before making adjustments.
مشاكل انقطاع الألياف
Fiber breaks represent one of the most common and disruptive problems in fiber manufacturing. These breaks can occur at any point in the drawing process, from the furnace exit to the take-up reel. Understanding the different types of breaks and their causes is essential for effective troubleshooting.
For a break near the furnace exit, preserve the time, preform identity, break location and preceding thermal, feed and tension records. Review relevant preform inspections and furnace alarms with the process owner. Do not diagnose ‘thermal shock’ or contamination solely from the break location. Inspection of the furnace or hot-zone components must follow the manufacturer’s safe shutdown and maintenance procedure.
For a suspected tension-related break, compare the tension trace with capstan speed, dancer position, reel events and the recorded break time. First confirm the measurement location and signal validity. A tension change after the fiber has broken may be a consequence, not its cause. Have qualified personnel review the evidence before changing control settings or inspecting the fiber path.
If breaks appear near coating or downstream handling equipment, retain representative samples and record their position relative to dies, guides, capstan and take-up. Check the applicable coating-geometry, cure, adhesion and mechanical-test results with the suppliers. Neither an eccentric coating nor a tacky surface alone proves the failure mechanism; compare the findings with the actual break evidence.
مشاكل التحكم في القطر
قد تؤدي اختلافات القطر إلى عدم صلاحية الألياف للاستخدام في التطبيقات الدقيقة. قد تحدث هذه الاختلافات على مسافات قصيرة (اختلافات دقيقة) أو مسافات طويلة (اختلافات كبيرة)، ويتطلب كل منها أساليب مختلفة لاستكشاف الأخطاء وإصلاحها.
Compare a diameter excursion with the identified preform, feed position and preform inspection records, but do not assume that a preform dimension transfers directly into the finished-fiber diameter. The drawing process and its control response also matter. Confirm the measured feature and units before comparing preform geometry, glass-cladding diameter or core geometry.
When investigating thermal conditions, compare the diameter trace with the furnace setpoint, measured temperature, power and relevant utility records. Distinguish the controller reading from the actual temperature of the glass. Check timing and measurement limitations before assigning a thermal cause or approving a recipe change.
For a suspected control problem, compare commanded and measured speed with the raw and filtered diameter signals. Ask the controls specialist to check sensor validity, delay, output limits and interactions between loops. Do not begin with arbitrary PID changes; use the approved trial procedure and retain before-and-after records.
If the diameter signal is periodic, compare its timing with known equipment cycles and environmental measurements. Check whether the pattern is present in an independent measurement or is an artefact of the gauge, filtering or sampling. A frequency match is an investigation lead, not proof that vibration or airflow caused the product defect.
استخدم هذه المصفوفة التشخيصية لجمع الأدلة قبل اختيار تدخل ما. إن عمليات التحقق فيها ليست أسبابًا مؤكدة ولا تعليمات تشغيل عالمية.
| Observed symptom | الأدلة التي يجب الحفاظ عليها | الفحوصات الأولى مع أخصائي المسؤول | Recovery evidence |
|---|---|---|---|
| انقطاع الألياف | موقع الكسر، الوقت، هوية البليت/البكرة والإشارات السابقة | تحقق من تتبع التوتر واربطه بالأحداث الحرارية وأحداث التغذية والمناولة | إعادة التشغيل المعتمدة بالإضافة إلى نتائج الهندسة والنتائج الميكانيكية والبصرية المطلوبة للمواد المتضررة |
| اختلاف القطر | تتبع المقياس الخام، والوحدات، وسجلات السرعة/التغذية وأوقات الأحداث | تحقق من صحة المقياس وافصل بين القطع الأثرية للقياس والتغيرات في العملية قبل الضبط | تم إثبات التسامح المتفق عليه للقطر تحت ظروف التجربة الموثقة |
| عيوب الطلاء | العينات، دفعة المادة، هندسة الطلاء، تسجيلات المعالجة والمناولة | تحقق من هندسة المُواصفات واختبارات المعالجة؛ راجع المحاذاة والتعرض فقط وفقًا لإجراءات المورِّد | النتائج التي تفي بمواصفات الطلاء المحددة، مع إمكانية التتبع إلى التجربة |
| زيادة التوهين | Test method, wavelength, sample identity, launch conditions and handling history | قم بتأكيد إعداد الاختبار وقابليته للتكرار قبل التحقيق في أسباب تتعلق بالمادة أو العملية | Repeatable results meeting the fiber specification and documented disposition of affected spools |
مشاكل تطبيق الطلاء
يمكن أن تؤثر عيوب الطلاء على الخصائص البصرية والميكانيكية للألياف النهائية. غالبًا ما تتطور هذه المشاكل تدريجيًا، مما يجعل الكشف المبكر أمرًا بالغ الأهمية لمنع ظهور كميات كبيرة من المنتجات المعيبة.
For a coating-dimension change, establish whether the measurement concerns total coated diameter, an individual layer or concentricity. Compare the validated trace with coating pressure, material temperature, lot history and die inspection records. The rate of change alone does not distinguish die wear from pressure, material or measurement issues.
When coating concentricity is outside the agreed limit, inspect fiber centering, die alignment and the measurement setup using the supplier’s procedure. Record the geometry results and perform any required optical tests separately. Do not diagnose polarization-mode dispersion from coating eccentricity alone.
For a suspected cure problem, record the coating formulation and lot, light-source type, exposure conditions, line speed and any specified inerting conditions. Compare the agreed cure and mechanical tests with the qualified coating process. A tacky surface or brittle sample is a symptom, not a complete diagnosis. Do not prescribe more UV exposure or attribute cracking to excessive cure without the coating supplier’s assessment.
When adhesion or stripping results are out of specification, confirm the test method and sample conditioning before comparing material, surface-handling and cure records. Ask the coating supplier to assess retained samples. Record the evidence and disposition rather than assuming contamination or material degradation is the cause.
نهج استكشاف الأخطاء وإصلاحها المنهجي
Effective troubleshooting requires a systematic approach that considers all possible causes and uses data to guide the investigation. Start by reviewing when the problem began, the recorded operating conditions and any changes made before the symptom appeared.
يلعب تحليل البيانات دورًا حاسمًا في تحديد أنماط المشكلات. تكشف مخططات الاتجاهات عن تغيرات تدريجية قد لا تكون واضحة من القياسات الفردية. كما يُمكّن تحليل الارتباط من تحديد العلاقات بين مختلف المعايير التي تُشير إلى الأسباب الجذرية.
Use batch comparisons to narrow the investigation, not to assign blame. If an excursion occurs with one preform batch, check whether recipe, operator, instrument, equipment or environmental conditions also changed. Compare equivalent runs and record which alternative explanations the evidence actually excludes.
A fishbone diagram or five-why review can organize hypotheses, but the diagram is not proof of root cause. Assign an owner to each check, document supporting and conflicting evidence, and verify the approved corrective action against the agreed acceptance criteria. Continue monitoring after restart; one successful trial does not guarantee that the problem cannot recur.
استراتيجيات الصيانة الوقائية
تساعد برامج الصيانة الوقائية على تجنب العديد من مشاكل التصنيع الشائعة من خلال معالجة المشكلات المحتملة قبل أن تُسبب انقطاعات في الإنتاج. يجب أن تستند هذه البرامج إلى توصيات مُصنّعي المعدات، وبيانات الأعطال السابقة، ومتطلبات العمليات.
تشمل أنشطة الصيانة المجدولة المعايرة الدورية لأنظمة القياس، واستبدال المكونات المستهلكة، وتنظيف المناطق الحرجة. وينبغي أن يراعي جدول الصيانة الفترات الزمنية والاستخدامية لتحسين موثوقية المعدات.
يمكن لتقنيات مراقبة الحالة تحديد المشاكل الناشئة قبل أن تُسبب الأعطال. يكشف تحليل الاهتزاز عن تآكل المحامل أو مشاكل المحاذاة. يُحدد التصوير الحراري المشاكل الكهربائية أو مشاكل نظام التبريد. يكشف تحليل الزيت عن التآكل الداخلي في الأنظمة الهيدروليكية أو أنظمة التشحيم.
تضمن إدارة مخزون قطع الغيار توفر المكونات الأساسية عند الحاجة إليها للصيانة أو الإصلاحات الطارئة. يجب أن يشمل المخزون عناصر الصيانة الدورية وقطع الغيار الضرورية التي قد تتسبب في توقف العمل لفترات طويلة في حال عدم توفرها.
تضمن برامج التدريب فهم المشغلين وموظفي الصيانة للإجراءات الصحيحة وقدرتهم على التعرّف على العلامات المبكرة لتطور المشاكل. تُساعد التحديثات التدريبية المنتظمة على تعزيز المهارات وإدخال تقنيات أو تقنيات جديدة.
تتتبع أنظمة التوثيق أنشطة الصيانة، وسجل المشاكل، واتجاهات أداء المعدات. تساعد هذه المعلومات على تحسين جداول الصيانة، وتحديد المشاكل المتكررة، ودعم جهود التحسين المستمر.
خاتمة
تتطلب عملية تصنيع الألياف الأساسية الناجحة التحكم الدقيق في المواد والمعدات والعمليات على طول سلسلة الإنتاج بأكملها.
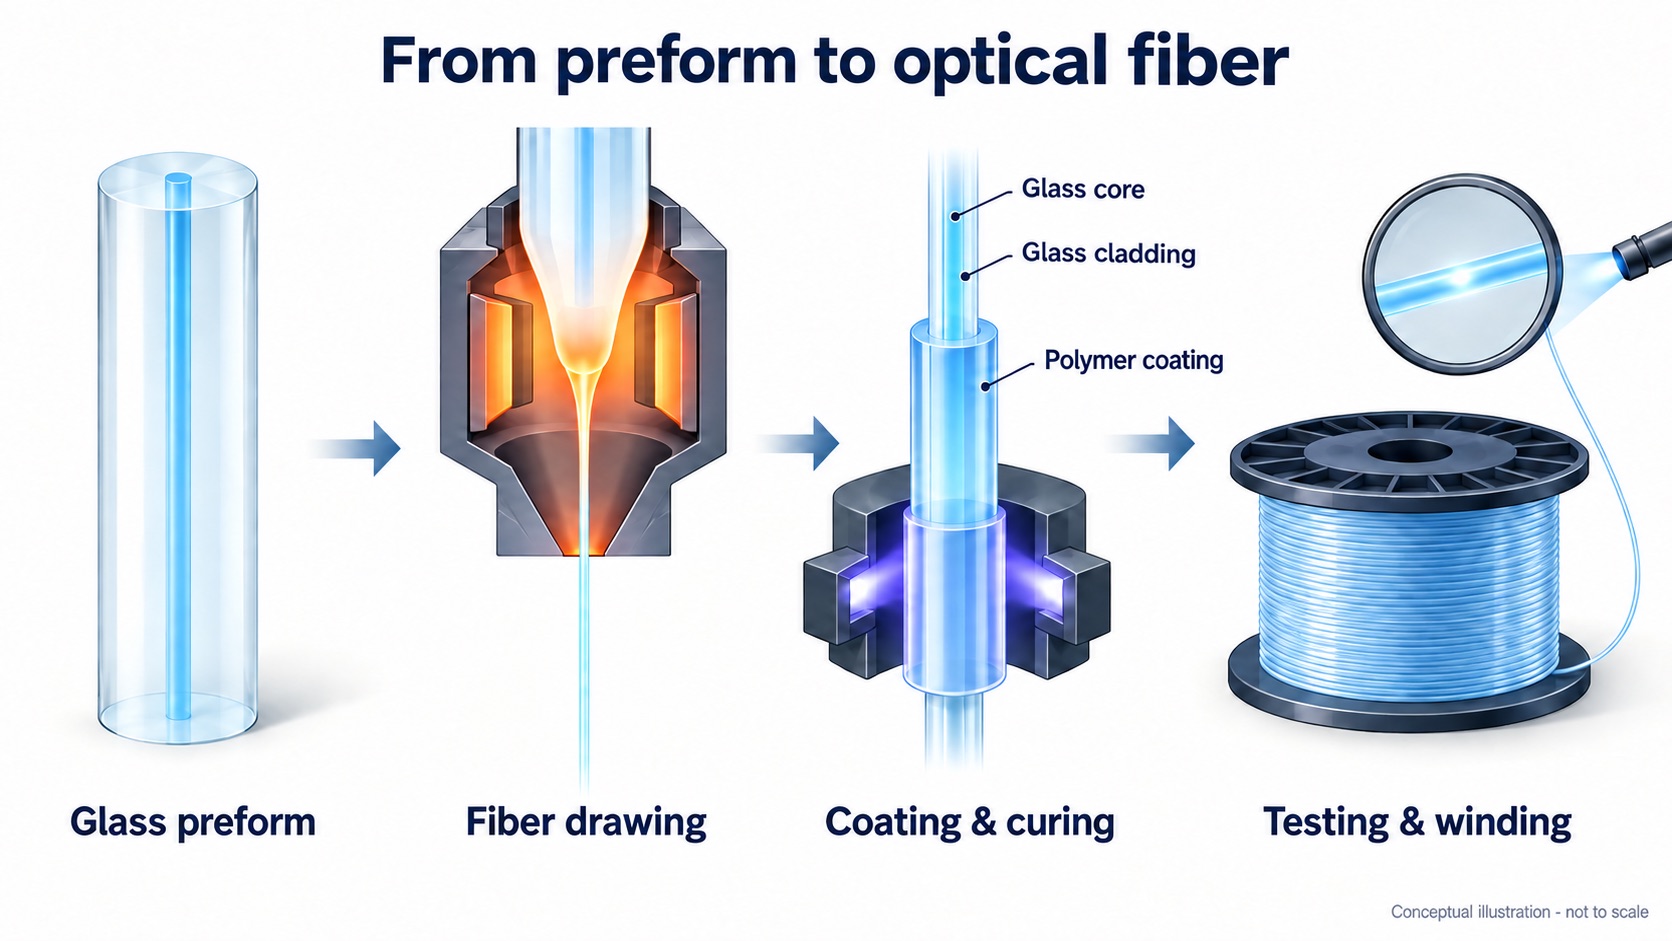
رسم توضيحي مفاهيمي لمراحل تصنيع الألياف البصرية الرئيسية؛ غير مُرسَم وفقًا للنسبة.
 English
 हिन्दी
 فارسی