


Cable Outer Sheath Extrusion Line
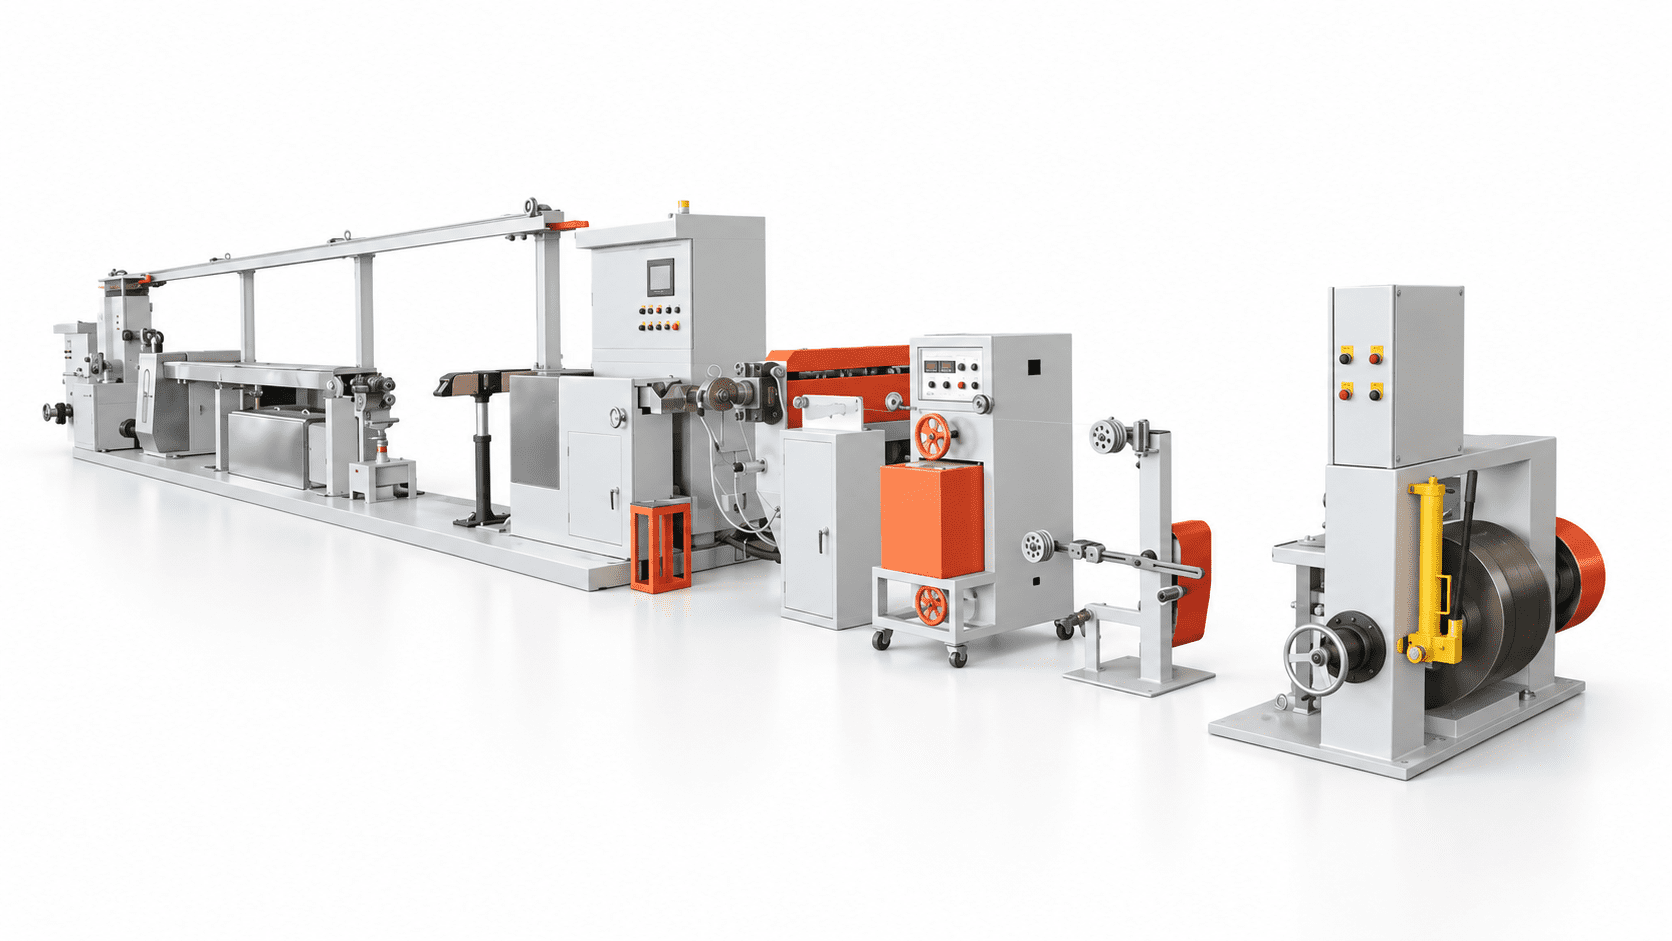
Extrude the protective outer jacket over a formed cable core. Match a PVC/PE sheathing line to your incoming cable, jacket thickness and finished diameter. Review the extruder together with cooling, haul-off and drum handling.
Extrude the protective outer jacket over a formed cable core
Match a PVC/PE sheathing line to your incoming cable, jacket thickness and finished diameter. Review the extruder together with cooling, haul-off and drum handling.
Position in your production line
LAN cable application. Outer sheathing receives the core from LAN cable-core assembly. Confirm the incoming diameter, jacket compound, wall thickness, finished diameter and take-up package, then match the accepted cable to the required coiling and packaging arrangement. Review the complete LAN production route; material-specific processing and the working output require project confirmation.
Compare the selection references
| Parameter | 70 | 80 | 90 |
|---|---|---|---|
| Screw diameter | Φ70 mm | Φ80 mm | Φ90 mm |
| Catalog extrusion capacity | 140 kg/h | 200 kg/h | 250 kg/h |
Catalog extrusion capacity is a mass-output reference, not cable line speed. Practical output depends on the compound, jacket section and complete line configuration.
Select around your actual product
Incoming cable
Supply the cable cross-section, construction and minimum/maximum incoming diameter.
Jacket specification
State PVC or PE grade, wall thickness, final diameter, tolerance and colour/layer requirements.
Output requirement
Provide the intended cable sizes and working speed. Compare extrusion capacity with the material demand of those constructions.
Drums and cooling
Confirm reel dimensions and weights, haul-off requirements, available cooling length and site utilities.
Define what your quotation includes
- Extruder, screw and selected PVC/PE processing arrangement.
- Crosshead, dies and agreed colour or layer options.
- Pay-off, cooling, haul-off and take-up.
- Printing, measurement and other specified line functions.
State whether this is a new line, an additional machine or an upgrade. Include existing equipment interfaces so the offer covers the connections that matter.
Continue your equipment selection
Core-Wire Insulation Extrusion Line
Configure the HK-UL-25–60 family for the required electrical or electronic wire construction. Match the material, layer arrangement, tooling and cooling to the finished insulation dimensions.
Cantilever Single Twisting Machine
Combine covered cores for control, communication and data-cable constructions. Select the cantilever size from the core dimensions, finished cable diameter, lay and take-up package.
Automatic Cable Coiling and Packaging Machine
Select the coiling and packaging arrangement from the cable construction, length per coil and finished package format. Define which measuring, cutting, tying and packing operations are included.
Explore the cable production equipment overview to place this machine in the wider production route.
Questions before choosing this machine
Does 250 kg/h mean a guaranteed cable speed?
No. Mass output and line speed are different quantities. The jacket cross-section, compound and operating conditions are needed to establish a production point.
Can this replace core-wire insulation extrusion?
Outer sheathing and conductor insulation are different duties. Use the incoming construction and wall requirements to select the correct extrusion route.
What does a complete sheathing offer include?
Confirm extrusion equipment and tooling together with pay-off, cooling, haul-off, take-up and the marking or measurement functions you require.
Tell us what you need.
Ask for a quotation, check a specification or get help selecting equipment.
EquipmentCable Outer Sheath Extrusion Line