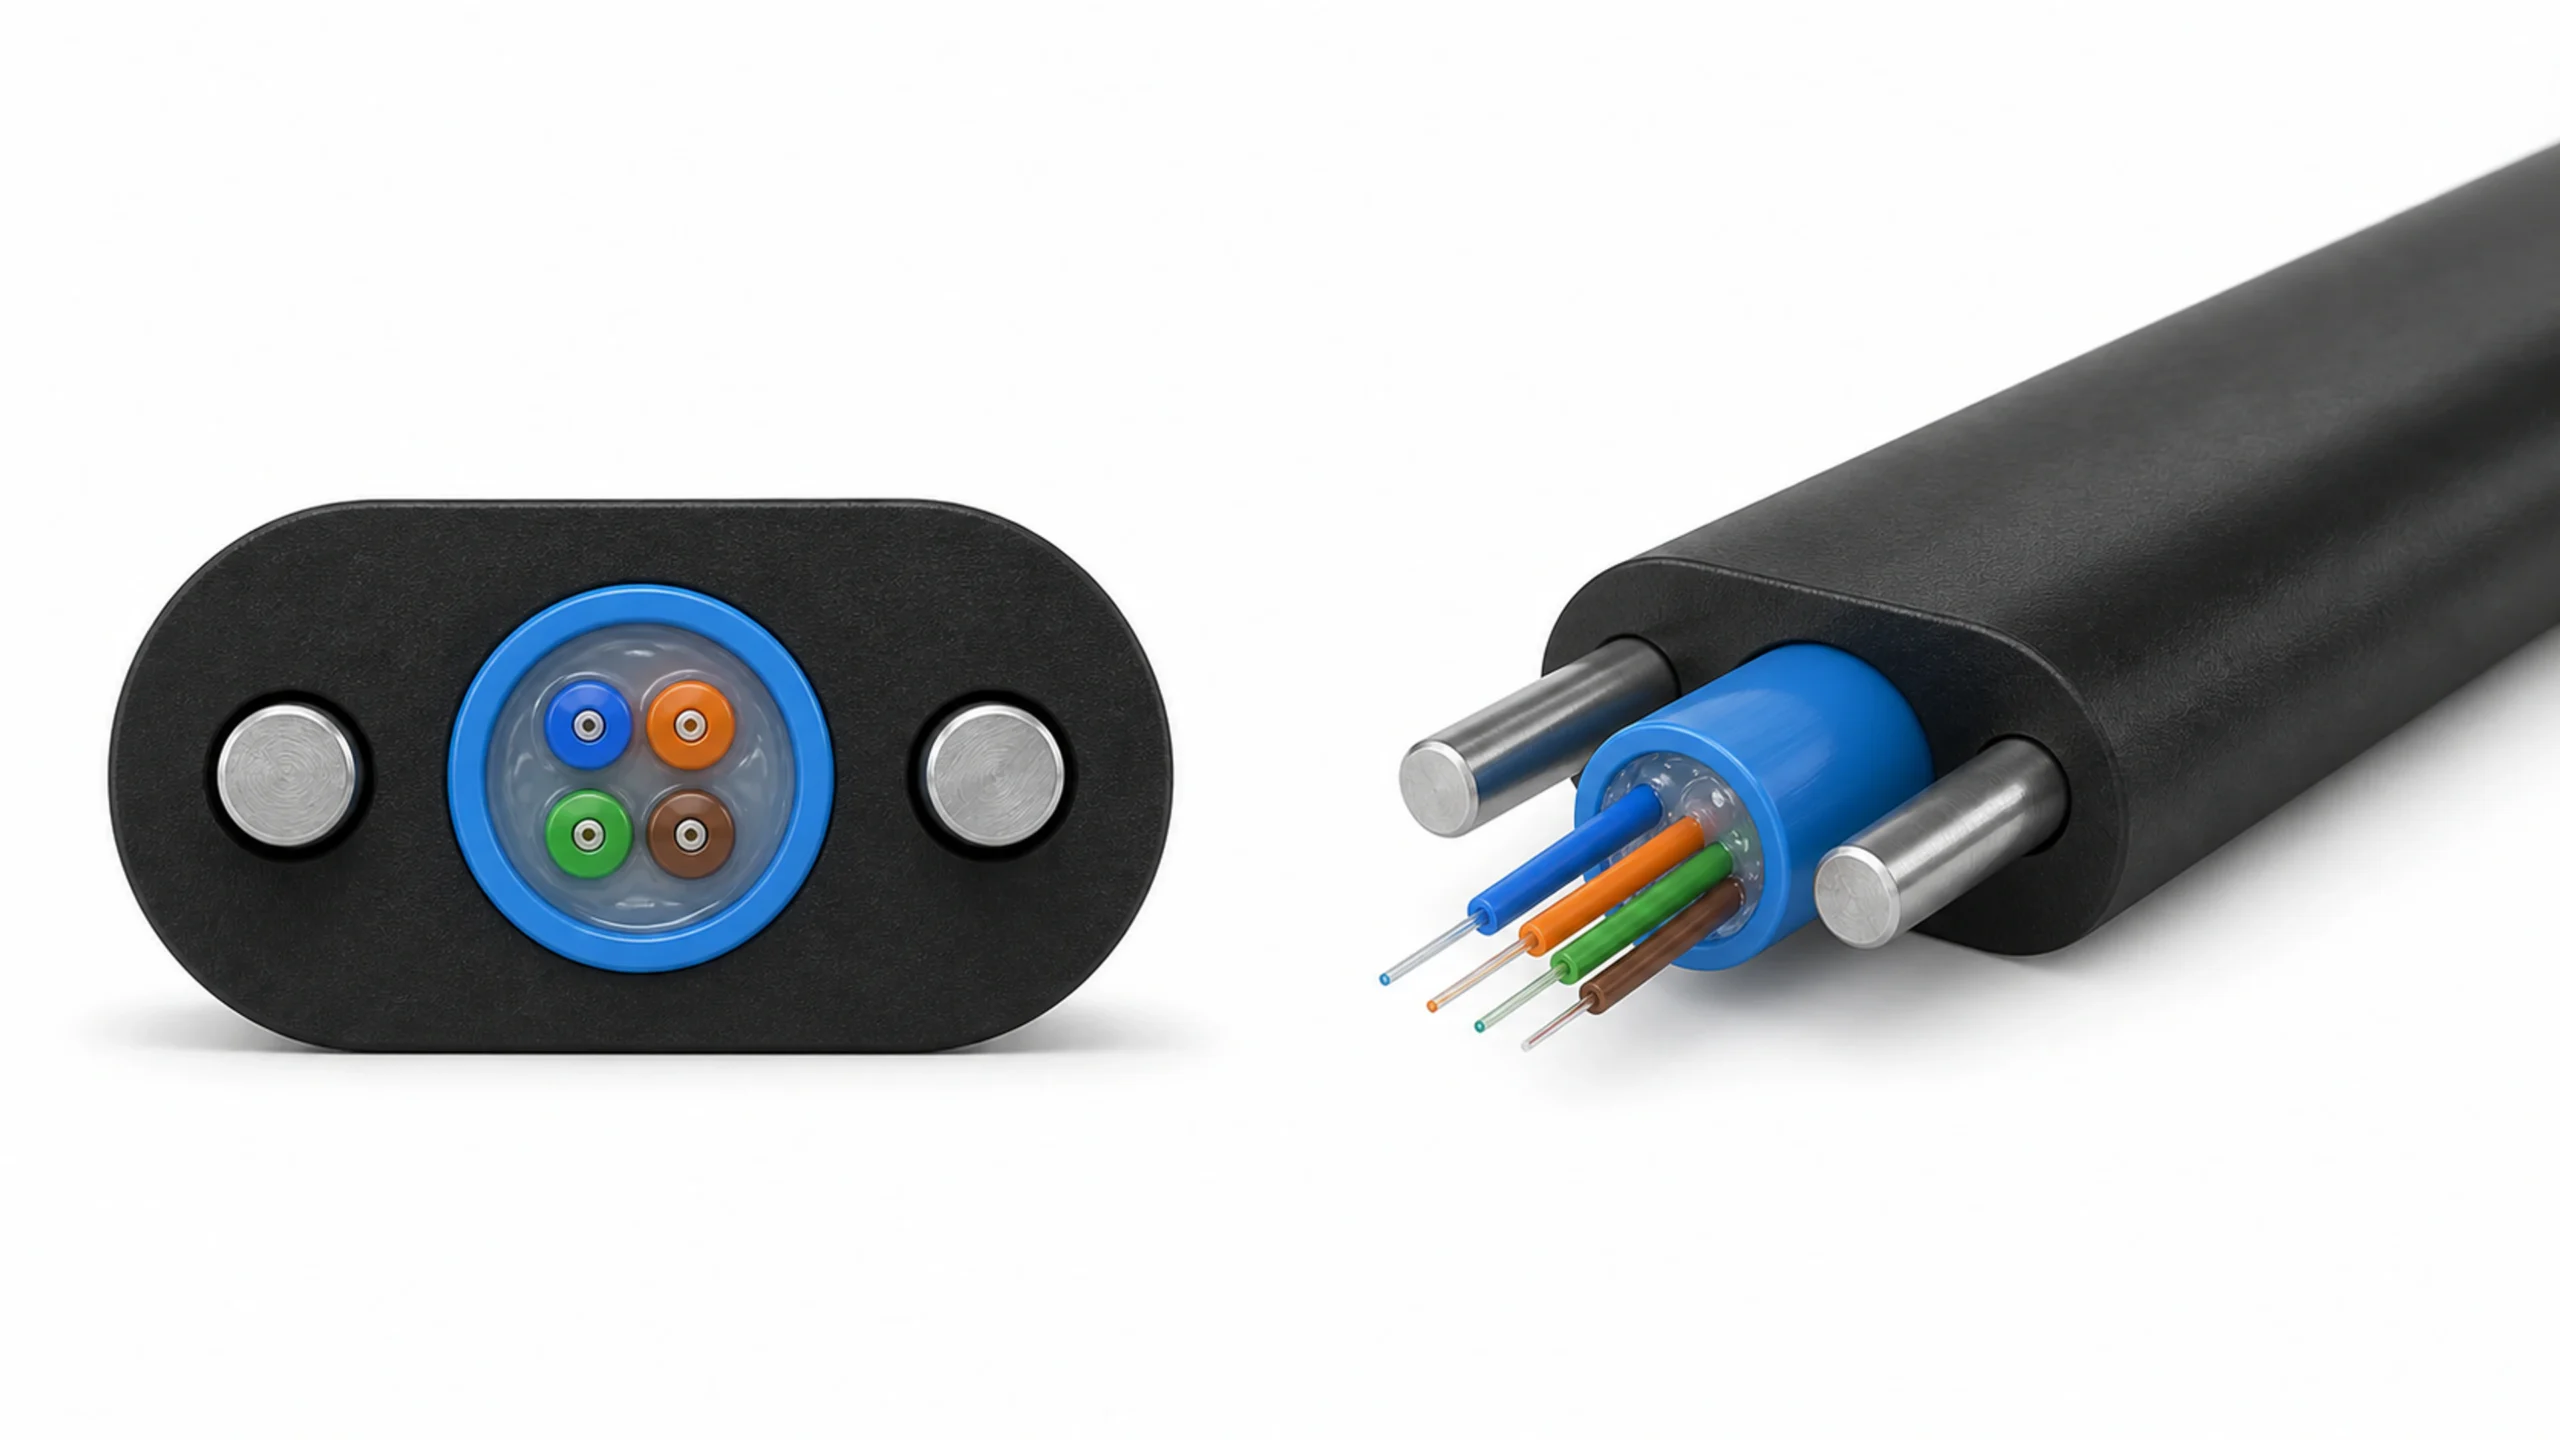
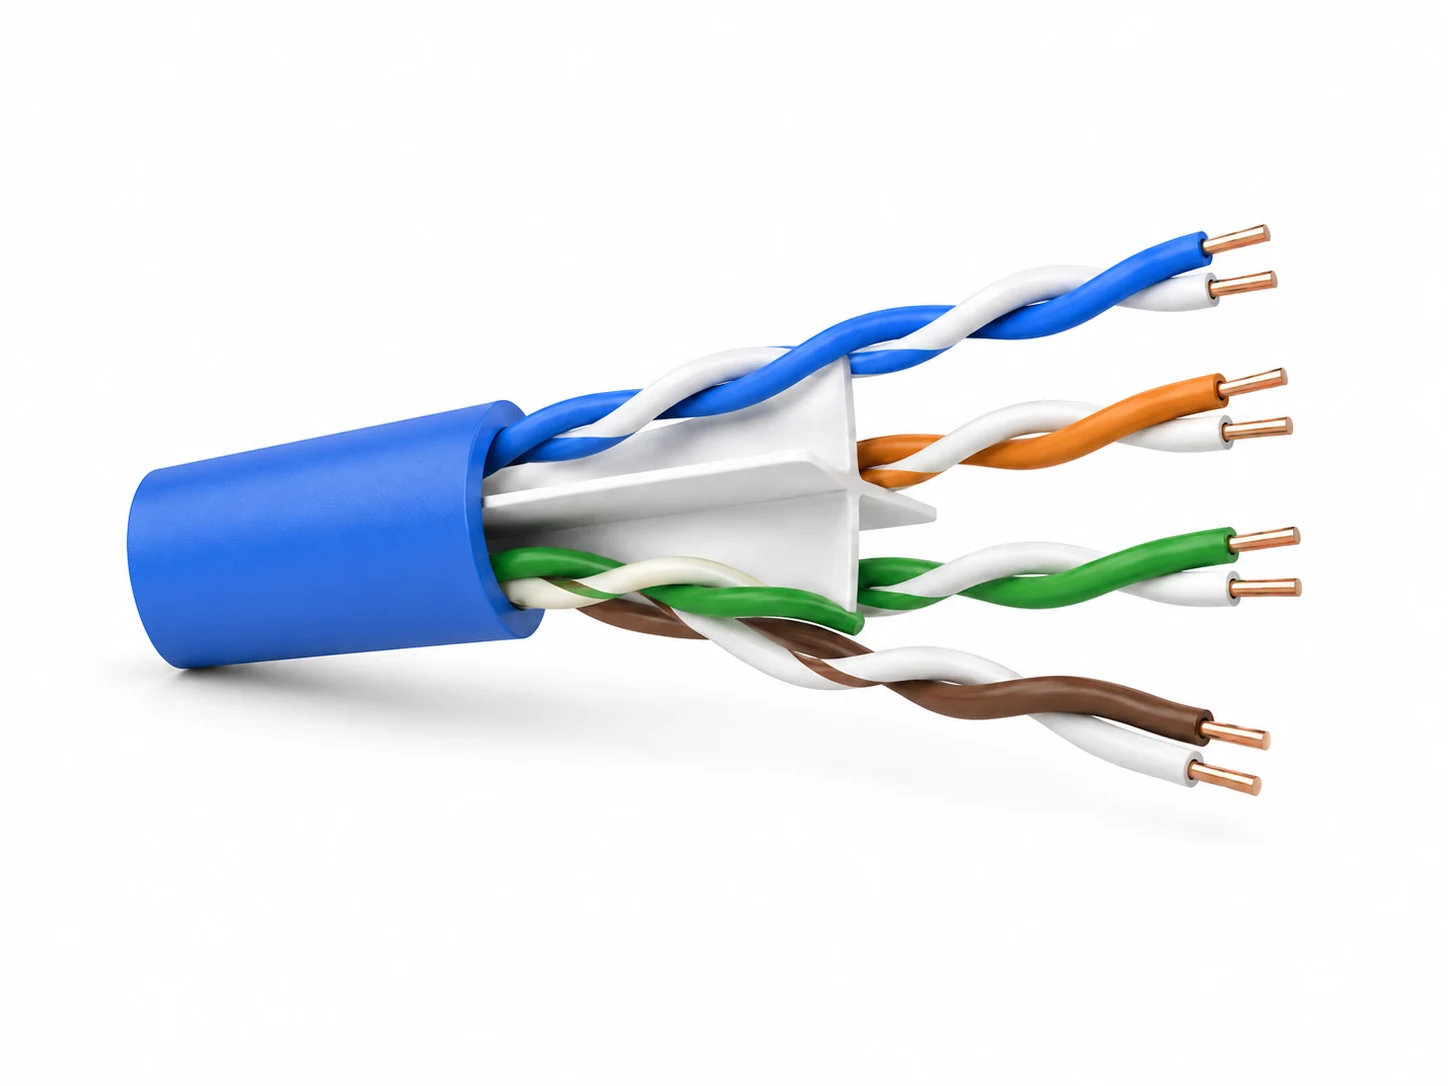
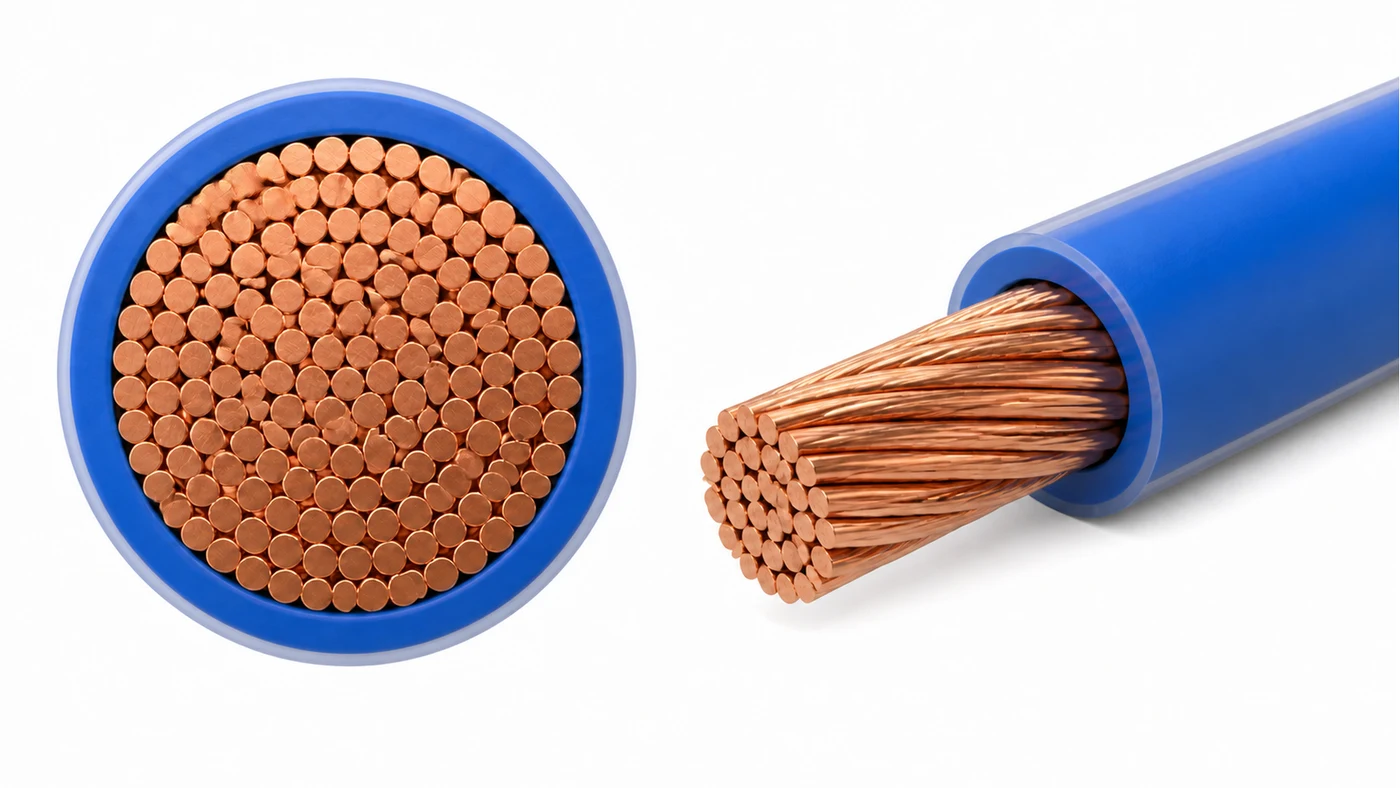
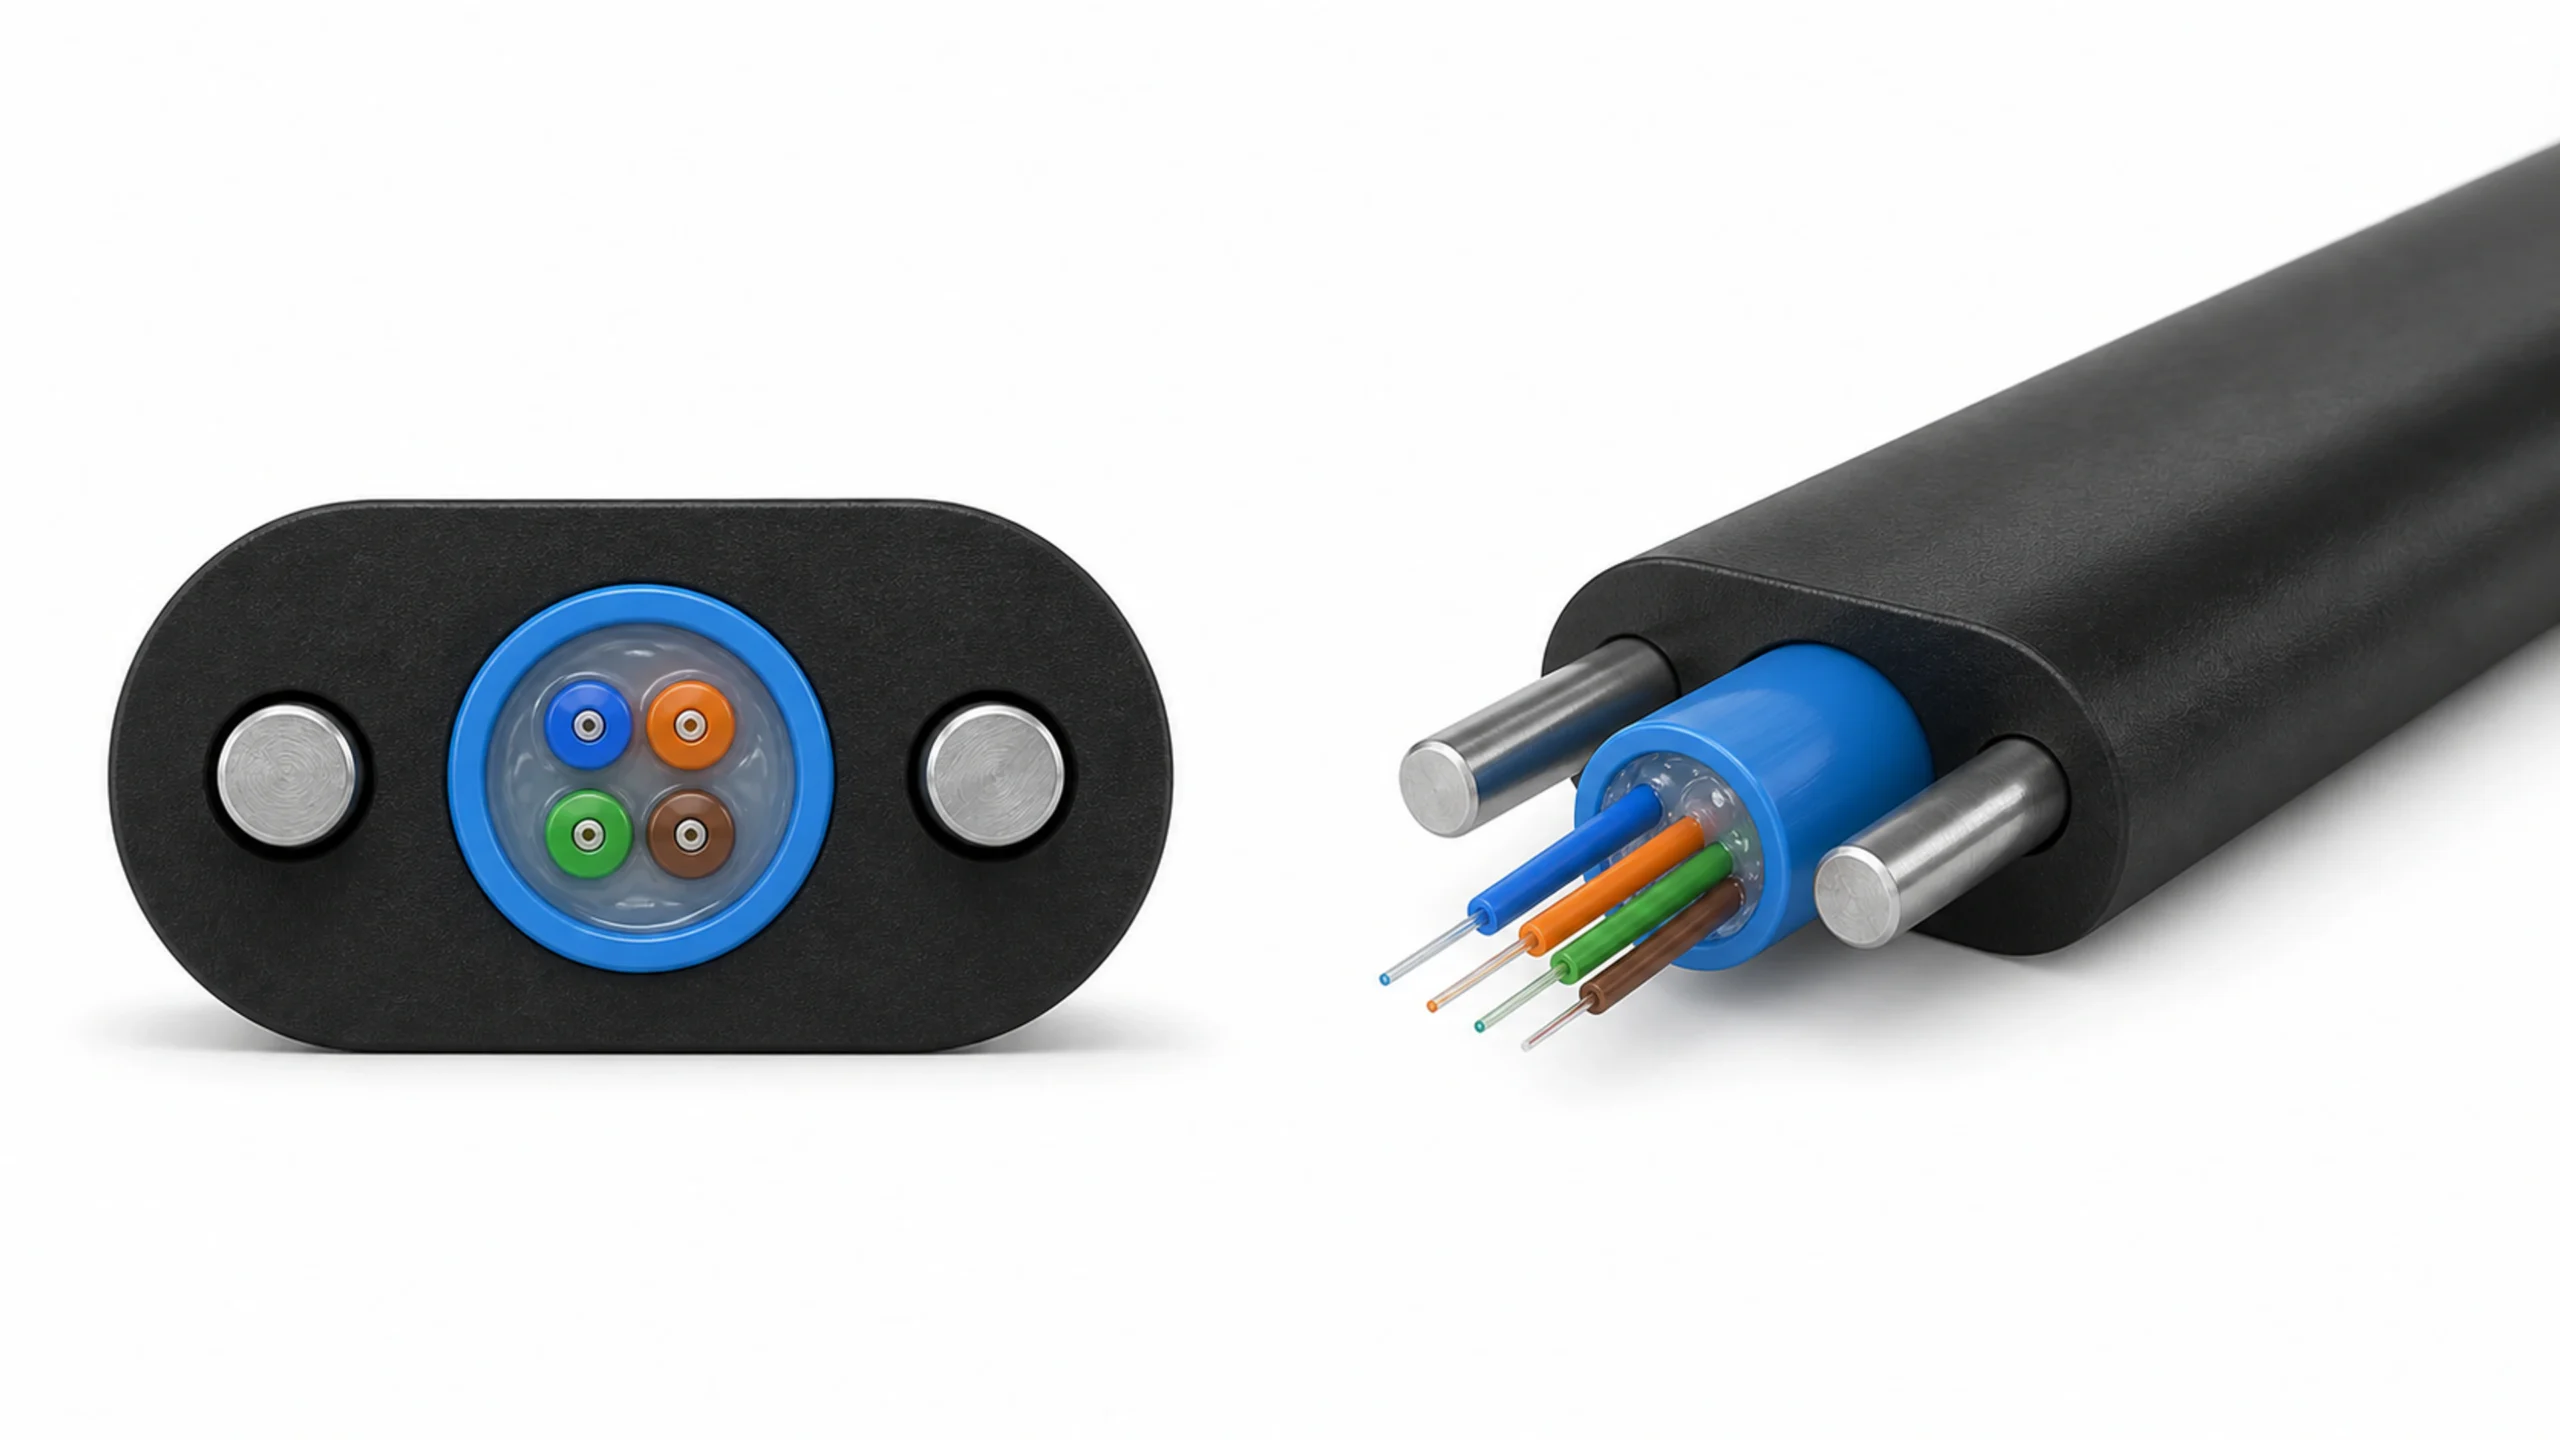
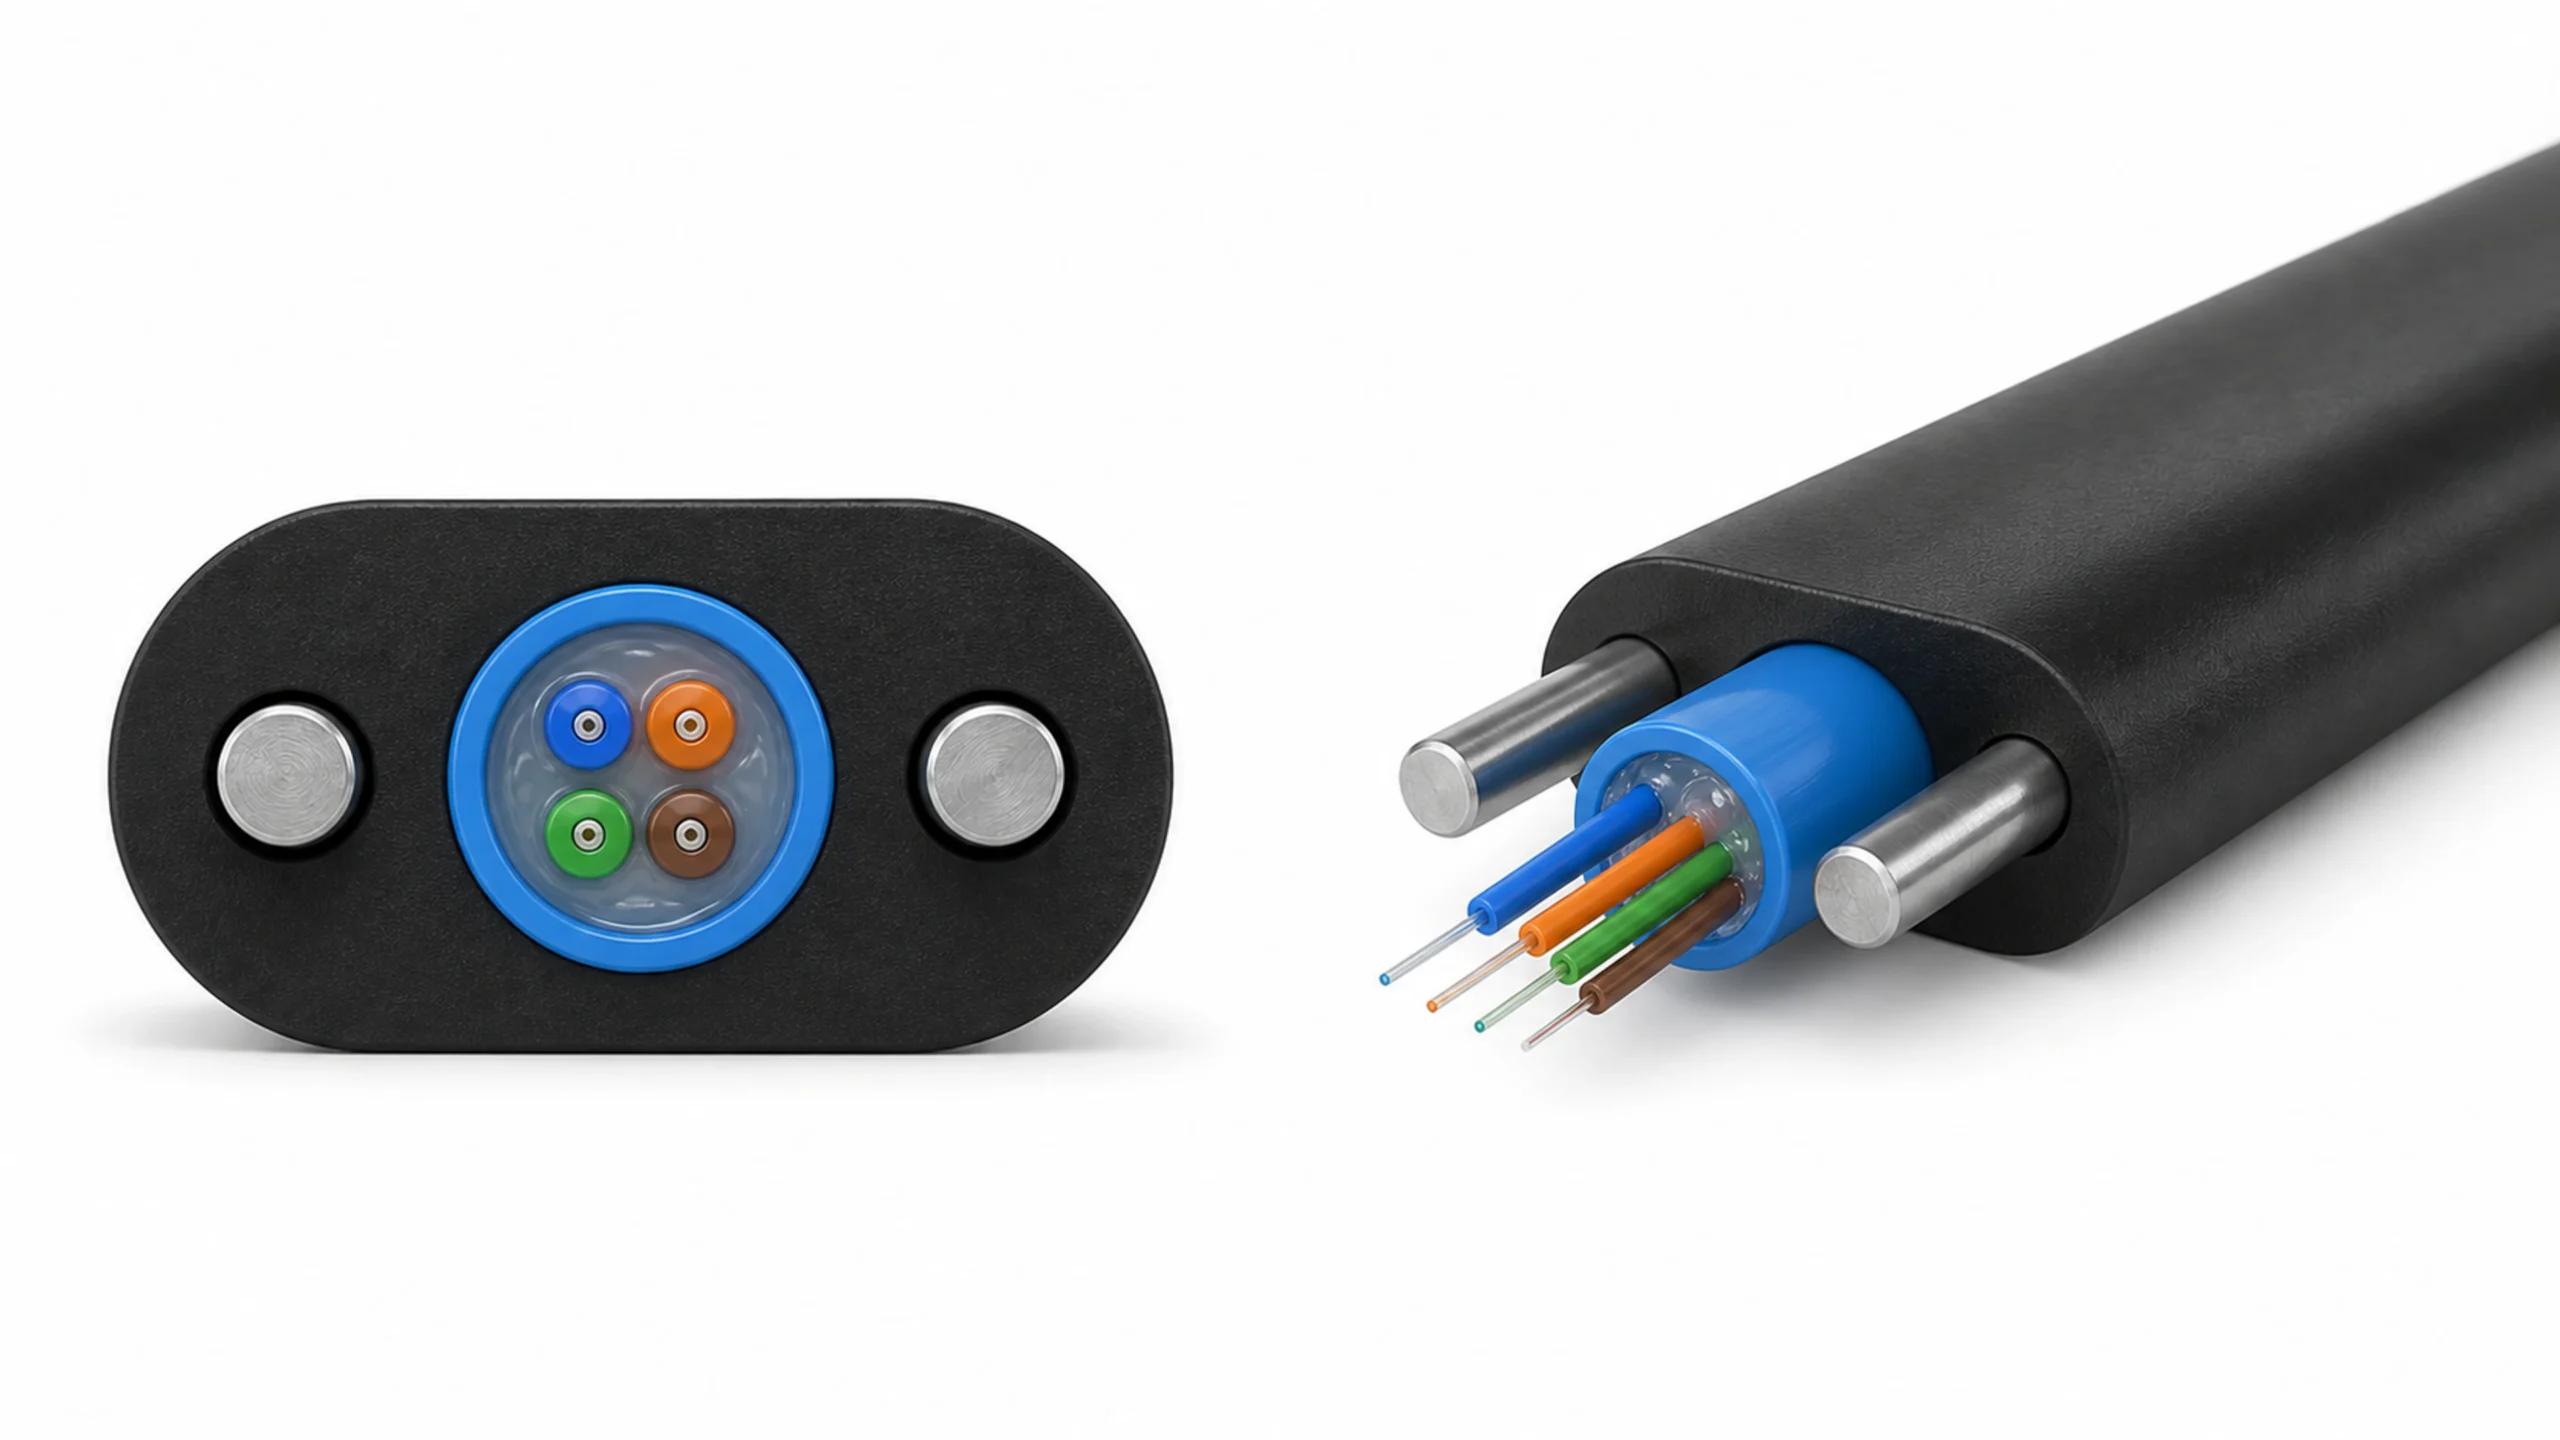

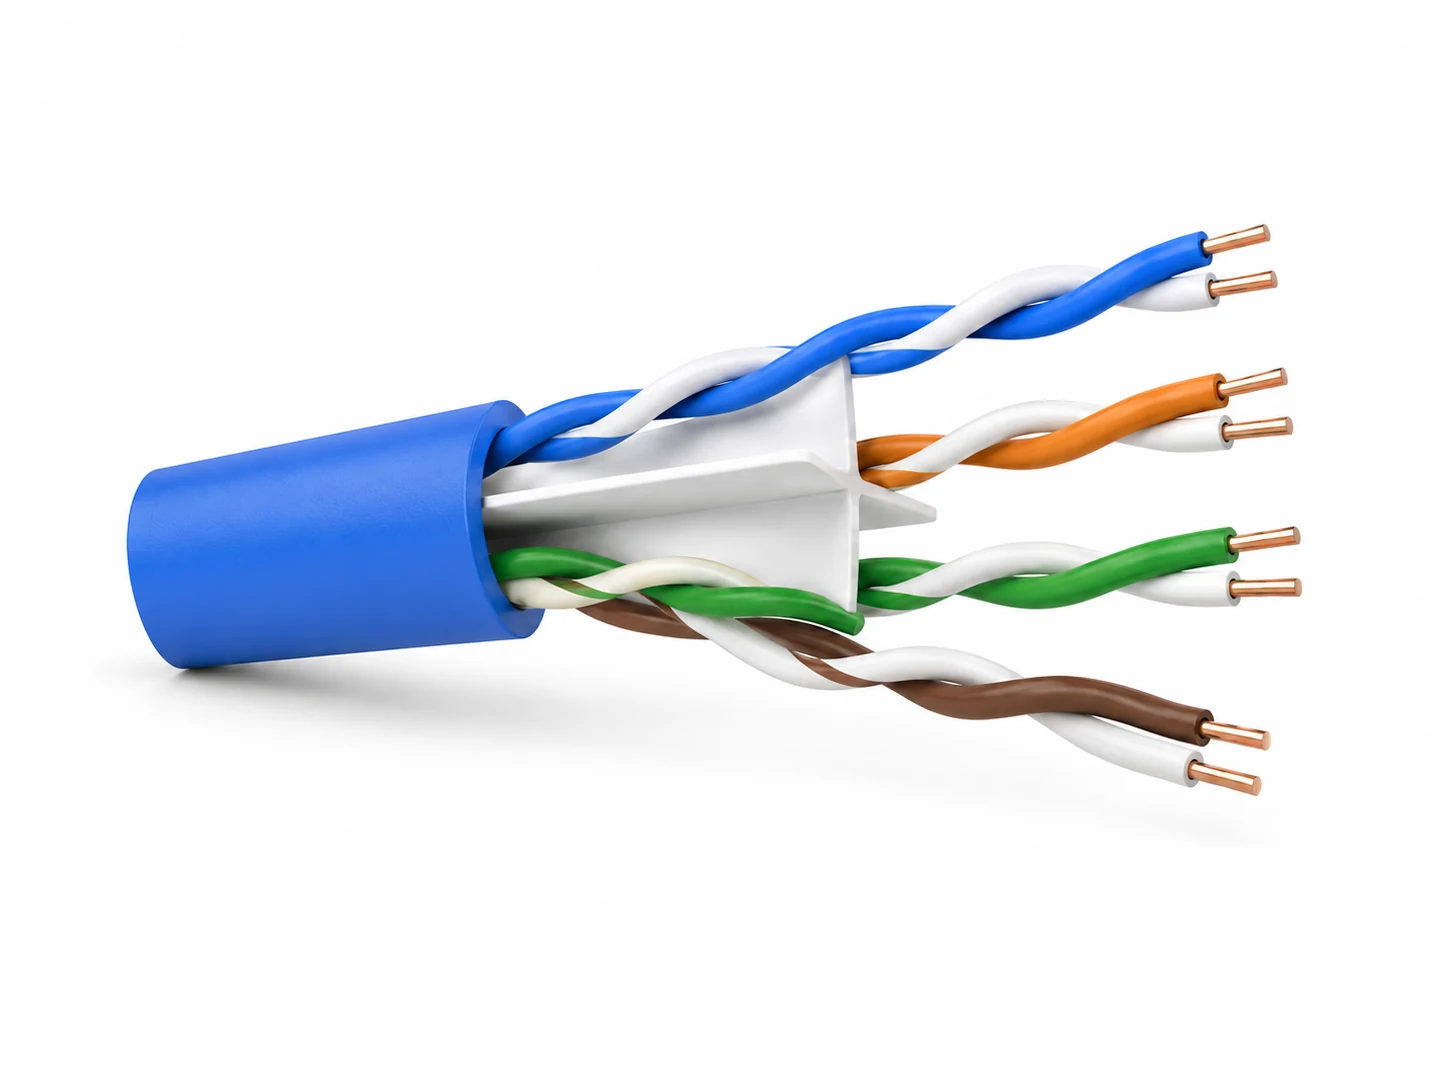
केबल संरचना पूर्वावलोकन
Reference cable
01
चयनित केबल समाधान
THHN / THWN तार उत्पादन लाइन
What is a THHN / THWN wire production line? It turns prepared copper conductors into PVC-insulated wire with a nylon covering. Form strands first when needed, then apply PVC and nylon, cool and dry the wire, inspect it and wind it to the agreed format.
- Cable designation
- THHN / THWN
- चालक सामग्री
- तांबा संदर्भ · पुष्टि करने के लिए अंतिम सामग्री
- चालक मार्ग
- पहले तार बनाएं—या तैयार कंडक्टर से शुरुआत करें
- Final configuration
- Φ800 buncher + Φ70 / Φ50 / Φ40 extrusion; scope to confirm
02 Cable definition
Define the THHN / THWN Wire Before Selecting Equipment
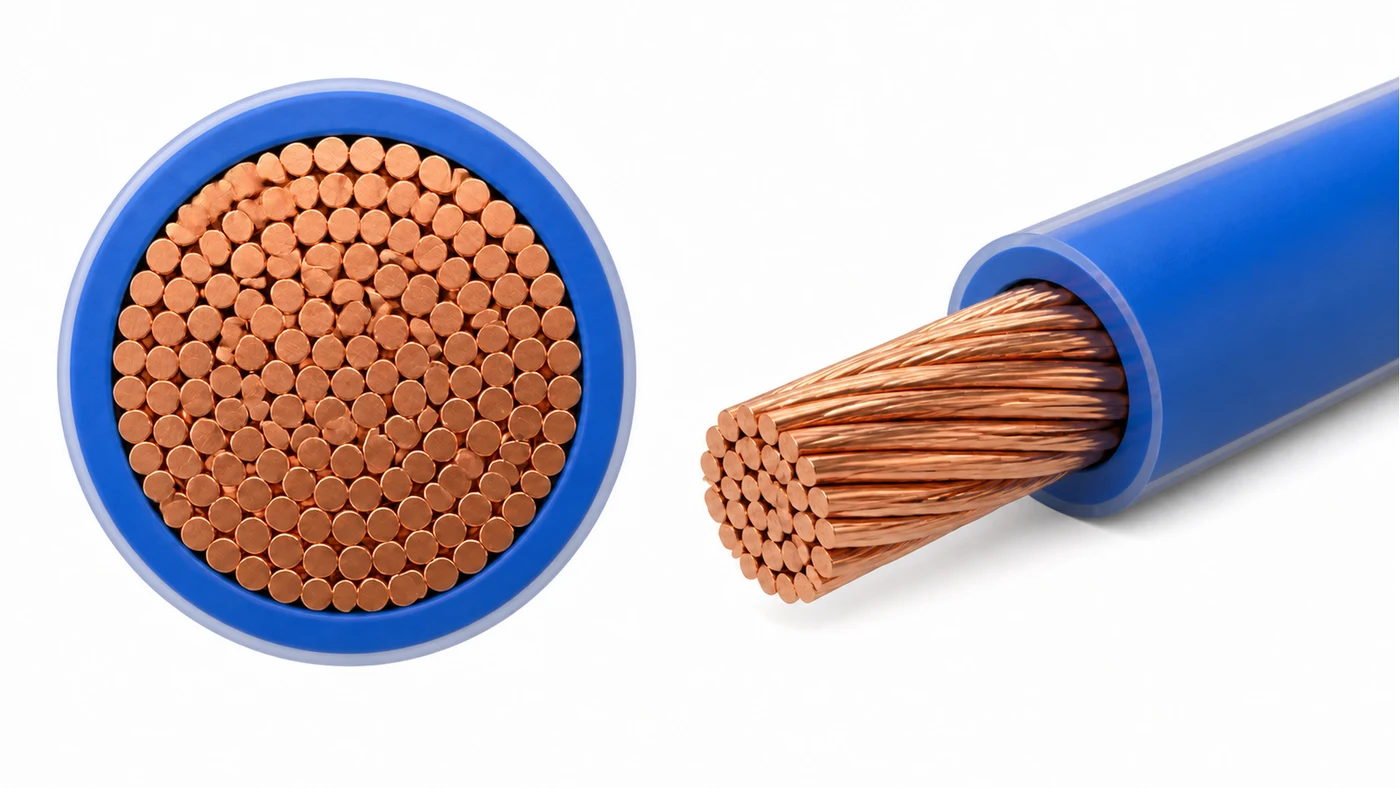
The image is a construction reference only. Confirm the copper conductor, PVC insulation and nylon covering, then define component-wire diameter, strand count and the dimensions of both material layers.
Known inputs and open confirmations
- Cable family
- THHN / THWN Wire
- Reference designations
- THHN / THWN for project review; THWN-2 only where specified and qualified
- चालक सामग्री
- Copper in this reference; an alternative conductor material requires separate review
- चालक निर्माण
- Solid, stranded or fine-stranded / flexible · To be confirmed
- व्यक्तिगत तार व्यास
- To be confirmed for a multi-wire conductor
- Number of wires / strands
- To be confirmed for each conductor
- Finished bare-conductor diameter
- To be confirmed before insulation extrusion
- Nominal conductor cross-section
- अभी पुष्टि के लिए
- Finished-product core count
- Single insulated core in this example. Strand count inside its conductor is a separate input.
- प्राथमिक इन्सुलेशन
- PVC insulation plus nylon covering; both compound grades to confirm
- PVC / nylon thickness and finished diameter
- Separate PVC and nylon thickness targets, tolerances and finished OD To be confirmed
- Rated voltage / final designation
- अभी पुष्टि के लिए
- लक्ष्य आउटपुट / क्षमता
- अभी पुष्टि के लिए
- स्वीकृति आधार
- अभी पुष्टि के लिए
स्ट्रैंड काउंट इंसुलेटेड केबल कोर की संख्या नहीं है।.
Specify the conductor as n × d mm: n is the number of individual wires and d is each wire’s diameter. Also confirm the finished bare-conductor diameter and nominal cross-section. Form the strands before insulation, or start with an approved ready-stranded conductor.
03 प्रारंभिक प्रक्रिया मार्ग
Match the Route to the Conductor Construction
This route illustrates single-core copper wire with PVC insulation and a nylon covering. Individual wires need forming; approved solid or ready-stranded conductors enter the PVC and nylon extrusion route.
Prepare wires if needed → Bunch / strand → PVC insulation / colour stripe → Nylon covering → Cool / dry → Inspect / mark → Take up
Confirm n × d, lay, bare-conductor diameter and resistance. Drawing / annealing and retail coiling / packing remain separate scope if required.
Typical process / not a fixed layout
Read the order, not a fixed machine spacing: conductor forming precedes PVC insulation and nylon covering. Feed, preheating and straightening are inside the extrusion package, not a separate process card. Surface drying precedes spark testing. Cooling, marking, gauges and accumulators follow the approved layout; a continuous mechanical link from buncher to extruder is not assumed.

Stage 02 / Required when forming strands
Bunching / Stranding
Form the specified individual copper wires into one bare conductor before insulation.
- इनपुट
- Prepared copper wires: wire count × individual-wire diameter.
- आउटपुट
- One bare stranded conductor with the specified lay, diameter and resistance.
- उपकरण स्रोत
- Reference equipment; model, manufacturer and supply scope to confirm
- Confirm
- The reference sheet lists 0.29–1.0 mm inlet wires and 2.5–16 mm² bunched area. Confirm the exact strand count, lay and finished bare-conductor diameter. Prepared solid or ready-stranded conductors bypass this stage.
04 आवश्यक चरण के अनुसार उपकरण
Review the Equipment Categories for This Route
Review each machine’s actual function, then confirm its model and interfaces. The Φ800 buncher and Φ70+50+40 extrusion specifications provide reference values, not a verified combined range. The 3D images are equipment-category references, not exact-model photographs.
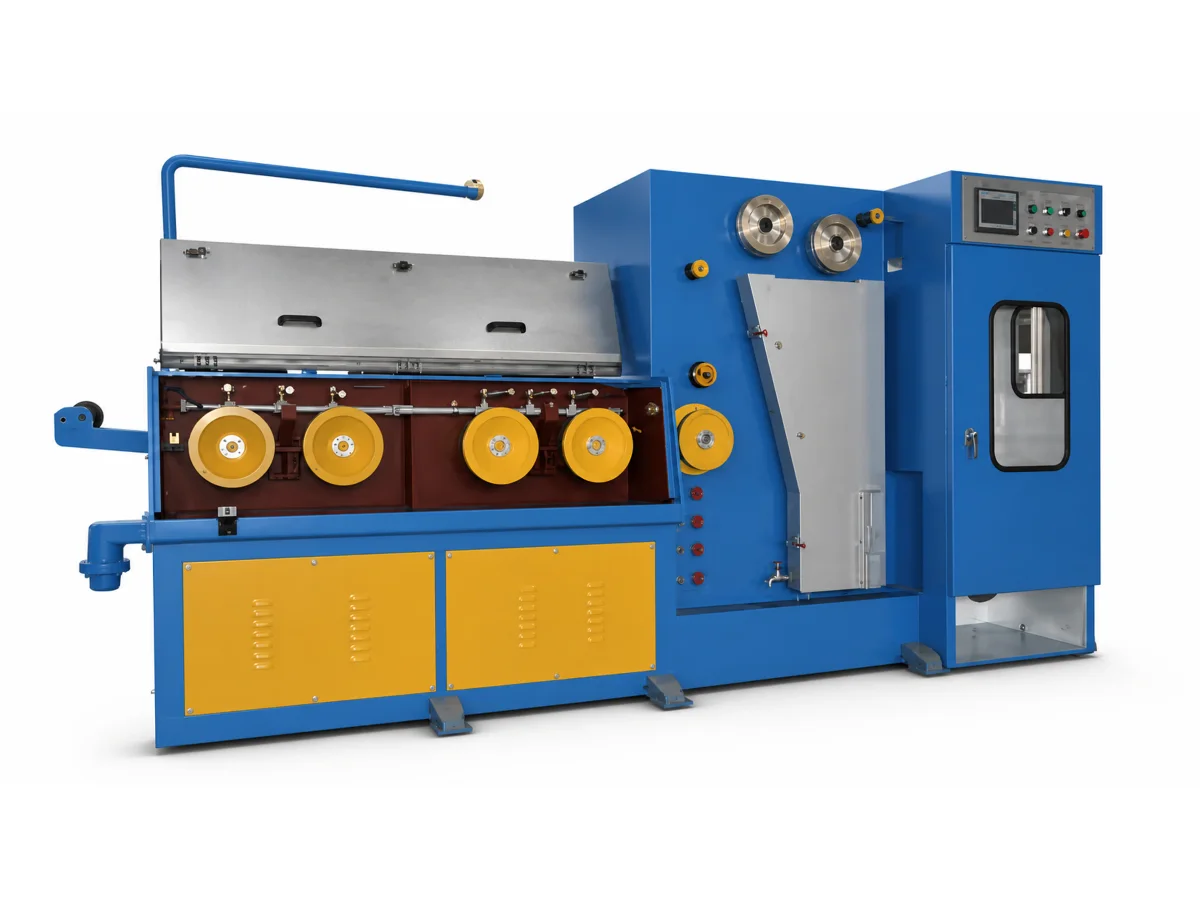 3D equipment reference · final model and configuration to confirm
01 / Upstream / as required
Drawing & Annealing
Reduce incoming copper rod or wire to the component-wire diameter. Include annealing where required to achieve the specified conductor condition; purchased wire may already meet these inputs.
Drawing and annealing are different functions. Confirm whether an annealer is integrated or separate; this reused image identifies only the drawing-equipment category. Drawing / annealing is not included in the two supplied reference packages.
07 Quality checkpoints
कंडक्टर, इंसुलेशन और फिनिश्ड वायर की जांच करें
Agree the inspection plan before equipment selection. These 3D references explain the checks; they are not factory photographs, customer cases or evidence of passed tests.
Conductor acceptanceConductor acceptance
नंगे कंडक्टर की जाँच करें
Confirm wire count, individual-wire diameter, lay, finished bare-conductor diameter and the specified conductor resistance.
Wire count inside one conductor is not the number of insulated cores. The 3D cable is a structure illustration, not a test sample.
 Dimensional control
व्यास मापें; दीवार सत्यापित करें
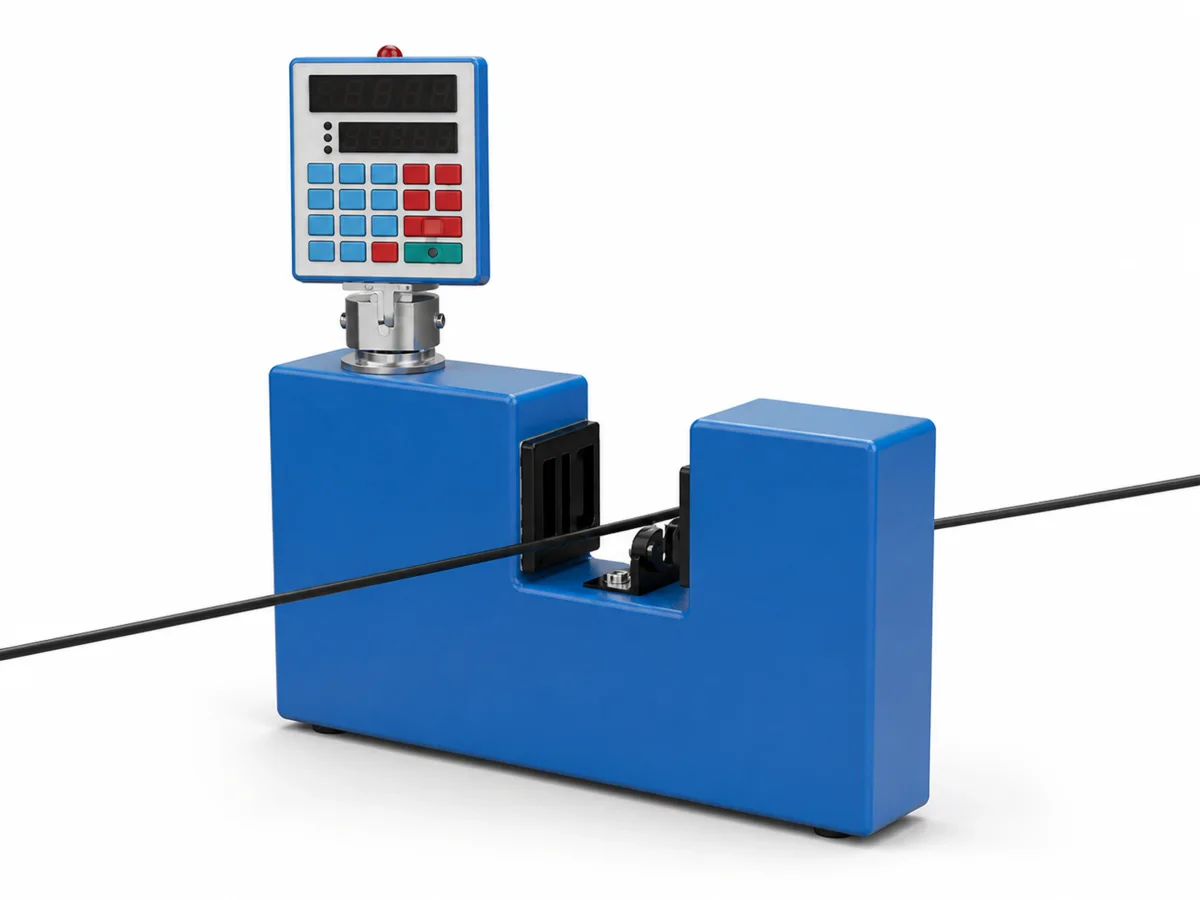
Monitor outside diameter during production. Verify PVC and nylon thicknesses separately, including minimum wall and eccentricity where required by the product specification.
एक लेजर बाहरी-व्यास गेज अकेले न्यूनतम दीवार मोटाई निर्धारित नहीं कर सकता। स्वीकृति विधि और सहनशीलताओं को परिभाषित किया जाना चाहिए।.
 In-line electrical check
Inspect the Dry Insulation
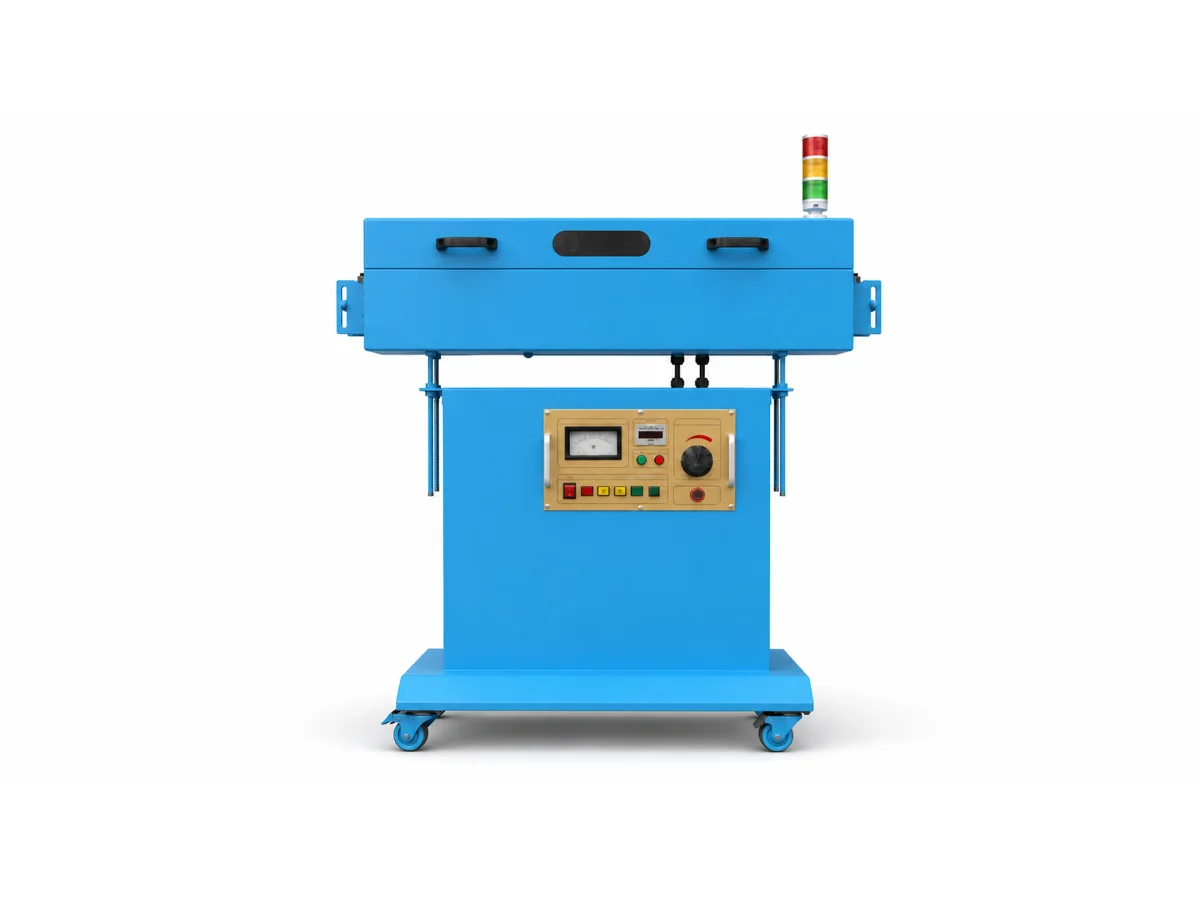
Dry the wire after cooling, apply the approved spark-test method and record or mark detected faults as specified.
Test type, voltage and response are product-specific. In-line spark testing is not a complete cable-certification test.
 Finished-product release
Confirm the Sale-Ready Package
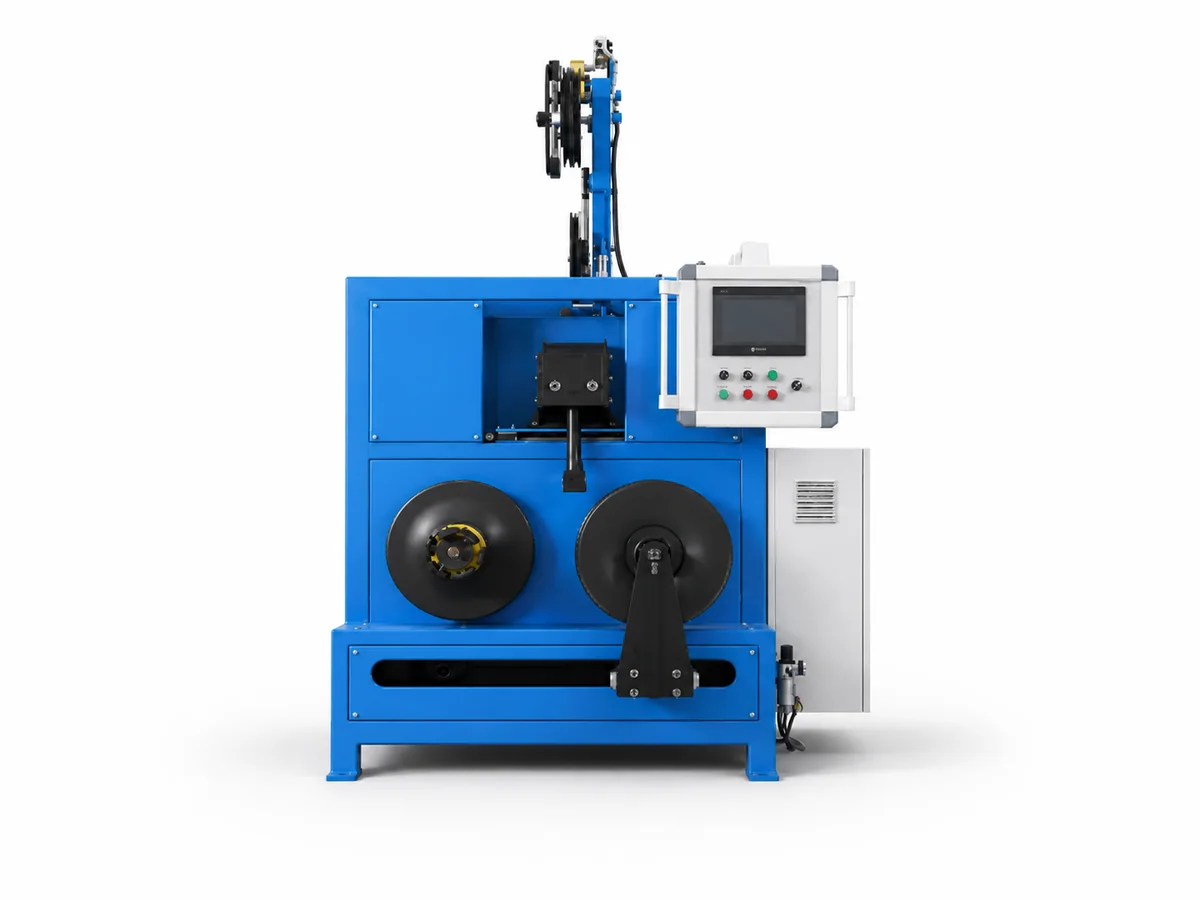
उत्पाद विशिष्टता द्वारा आवश्यक समझौता की गई लंबाई, अंकन, वाइंडिंग और पैकिंग के साथ-साथ तैयार तार के विद्युत, आयामी और सामग्री परीक्षणों की जाँच करें।.
The handling image is not an automatic packing-package claim. THHN / THWN qualification, test records and FAT/SAT evidence require actual project data.
Keep illustration and evidence separate. Add actual trial records, sample measurements and project acceptance documents once available. No performance or certification is inferred from a render.
आवश्यक परियोजना रिकॉर्ड English
 हिन्दी
 فارسی