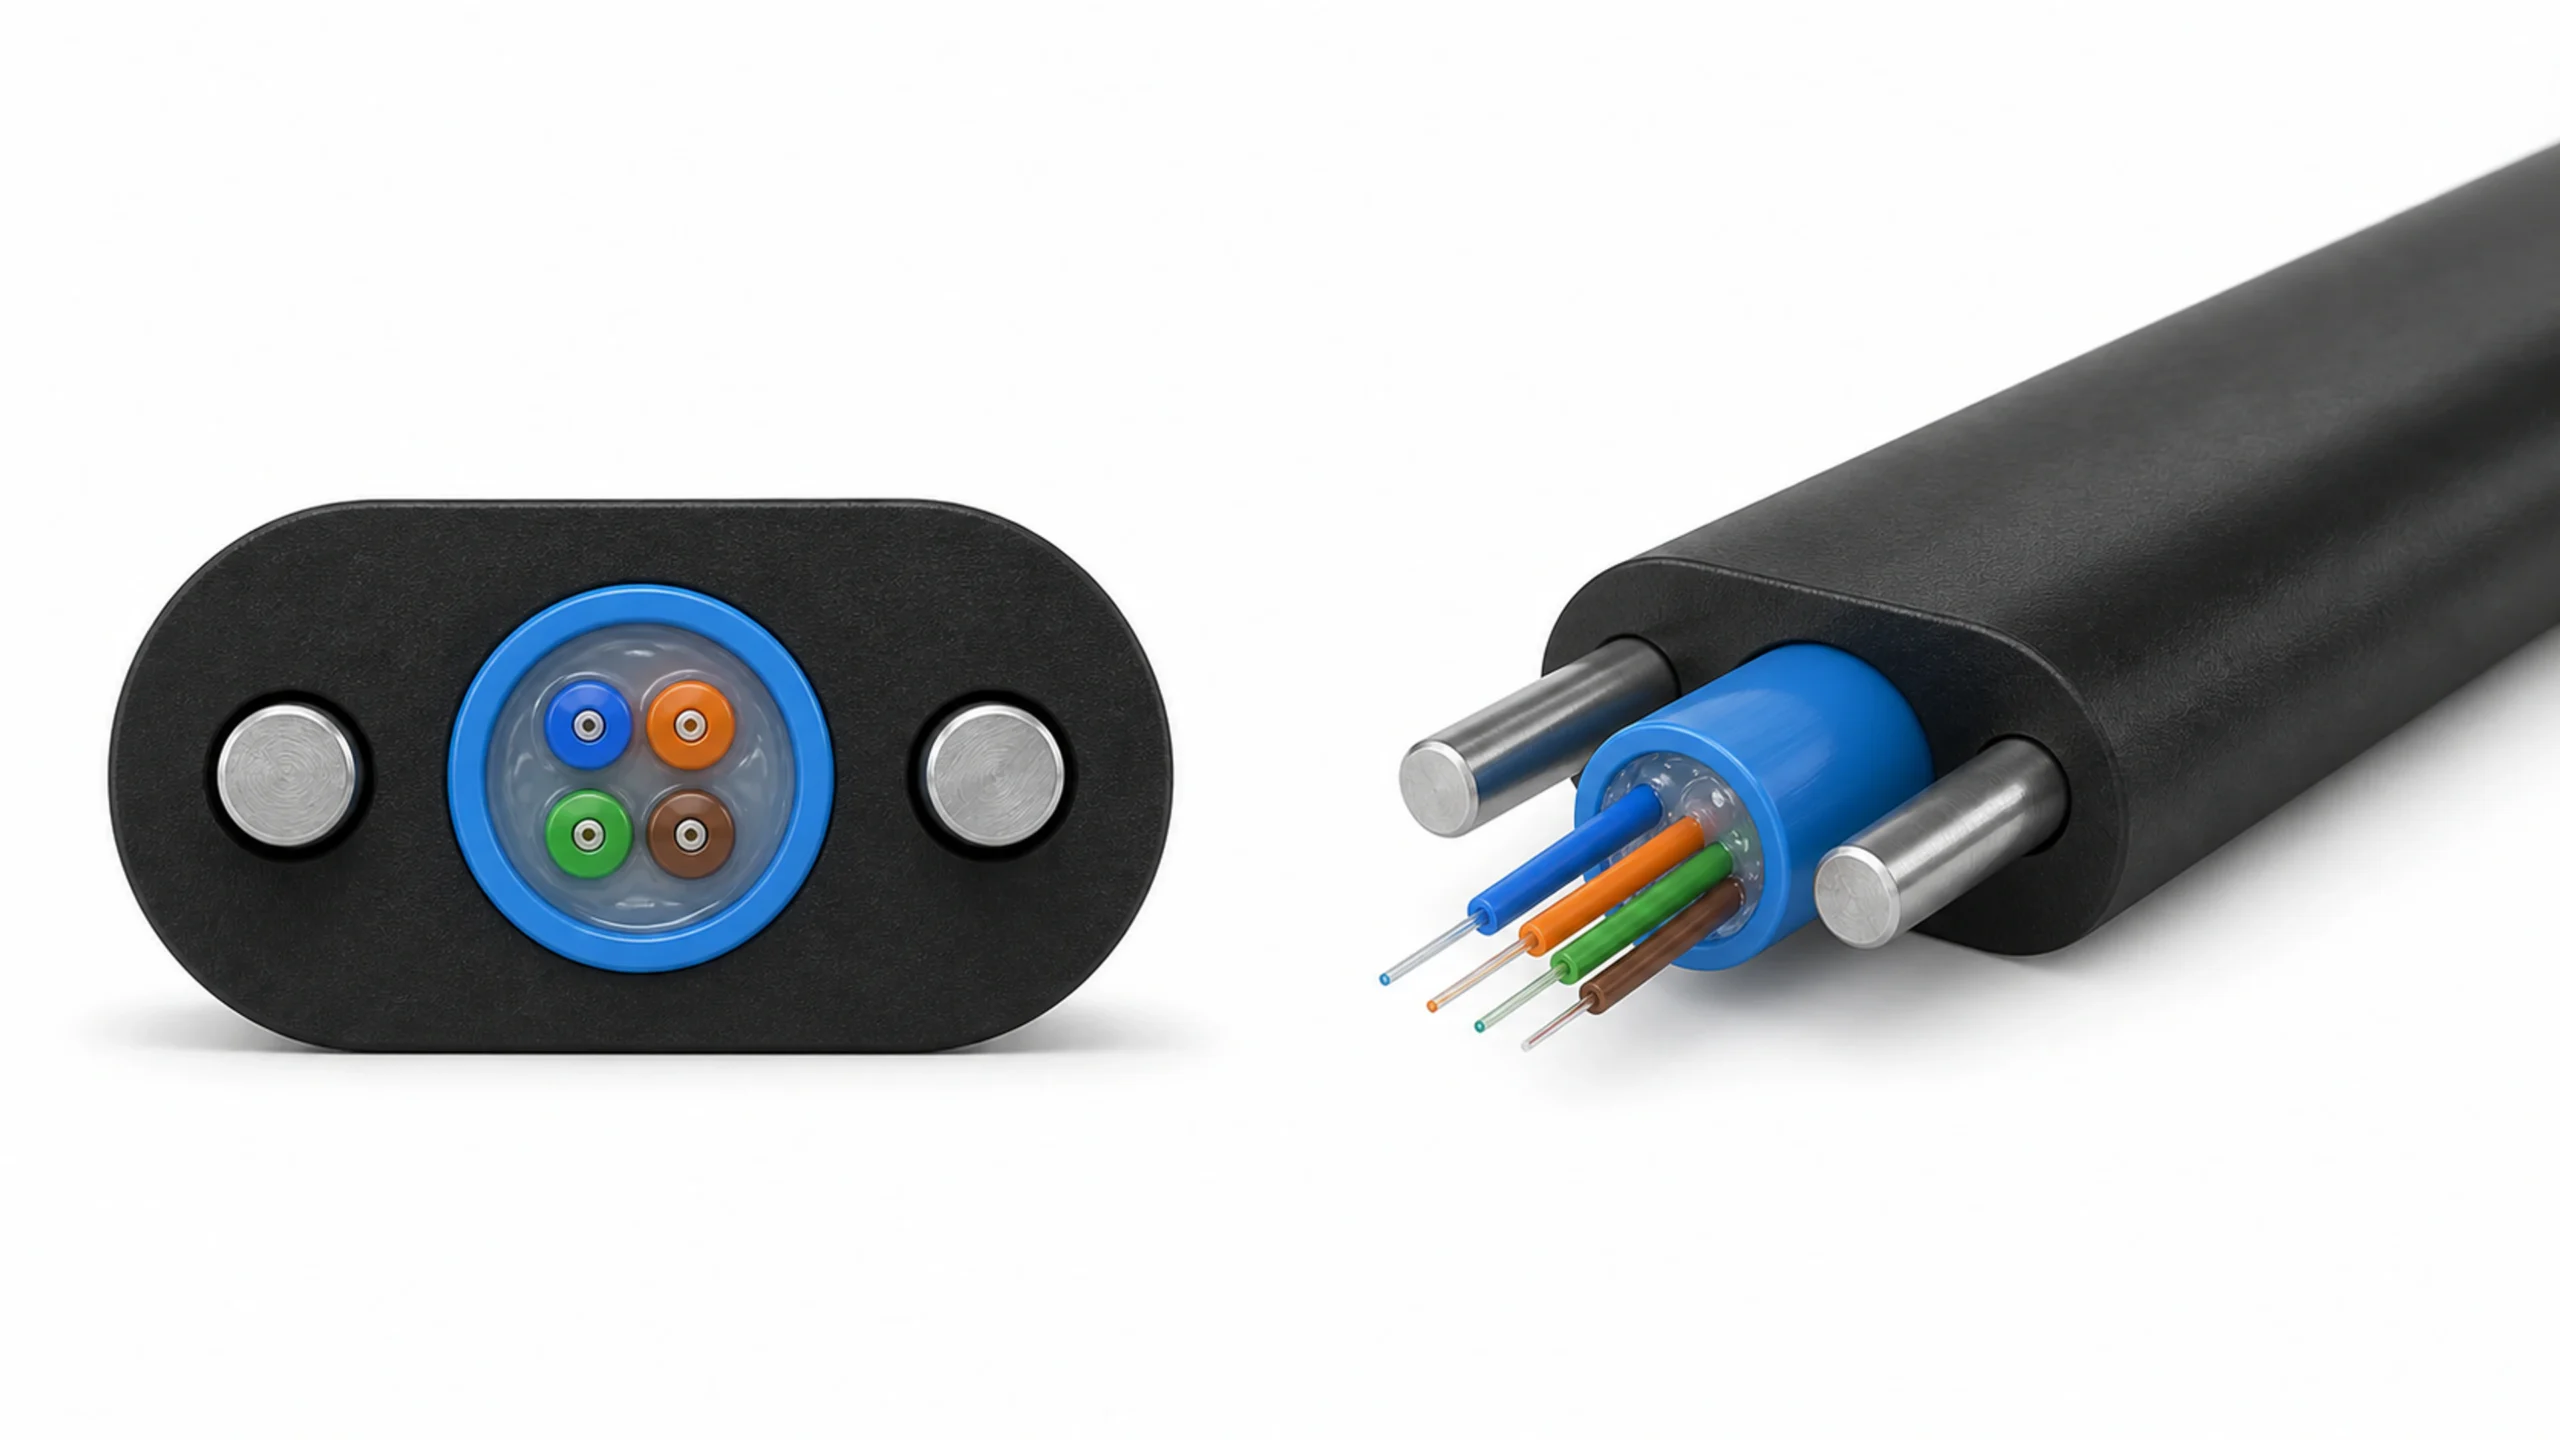
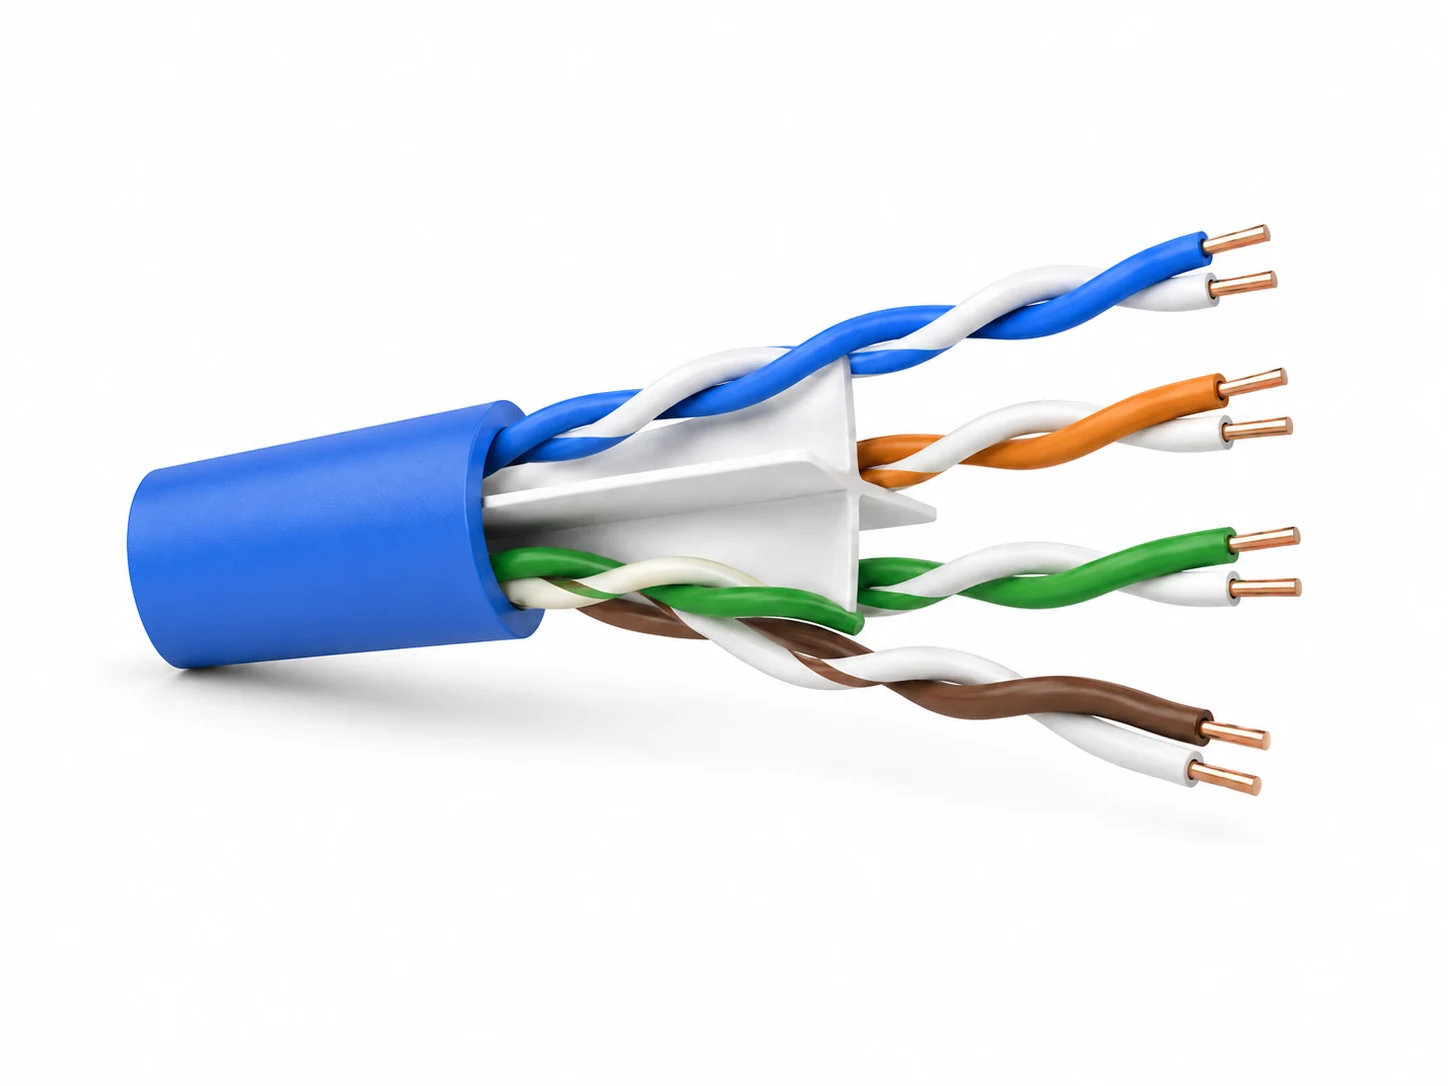
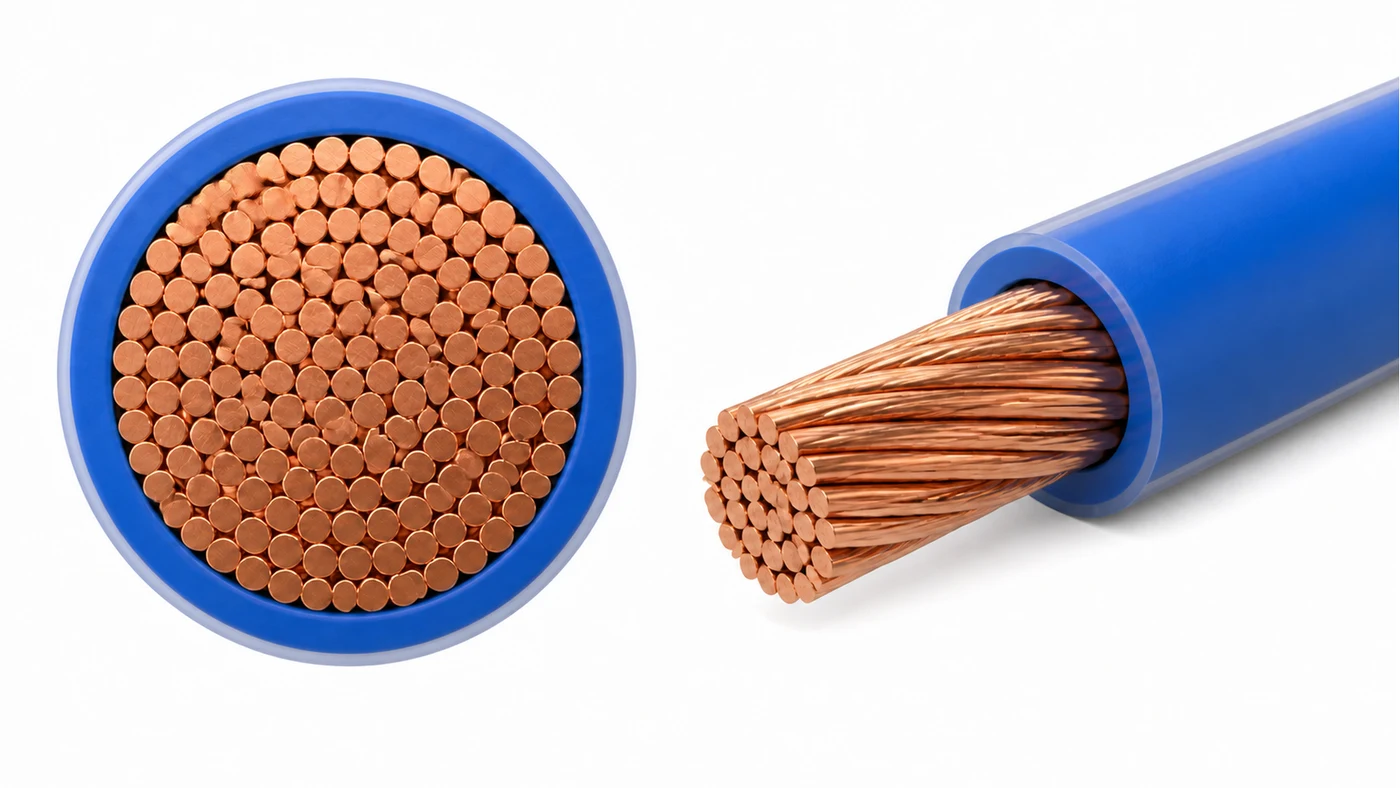
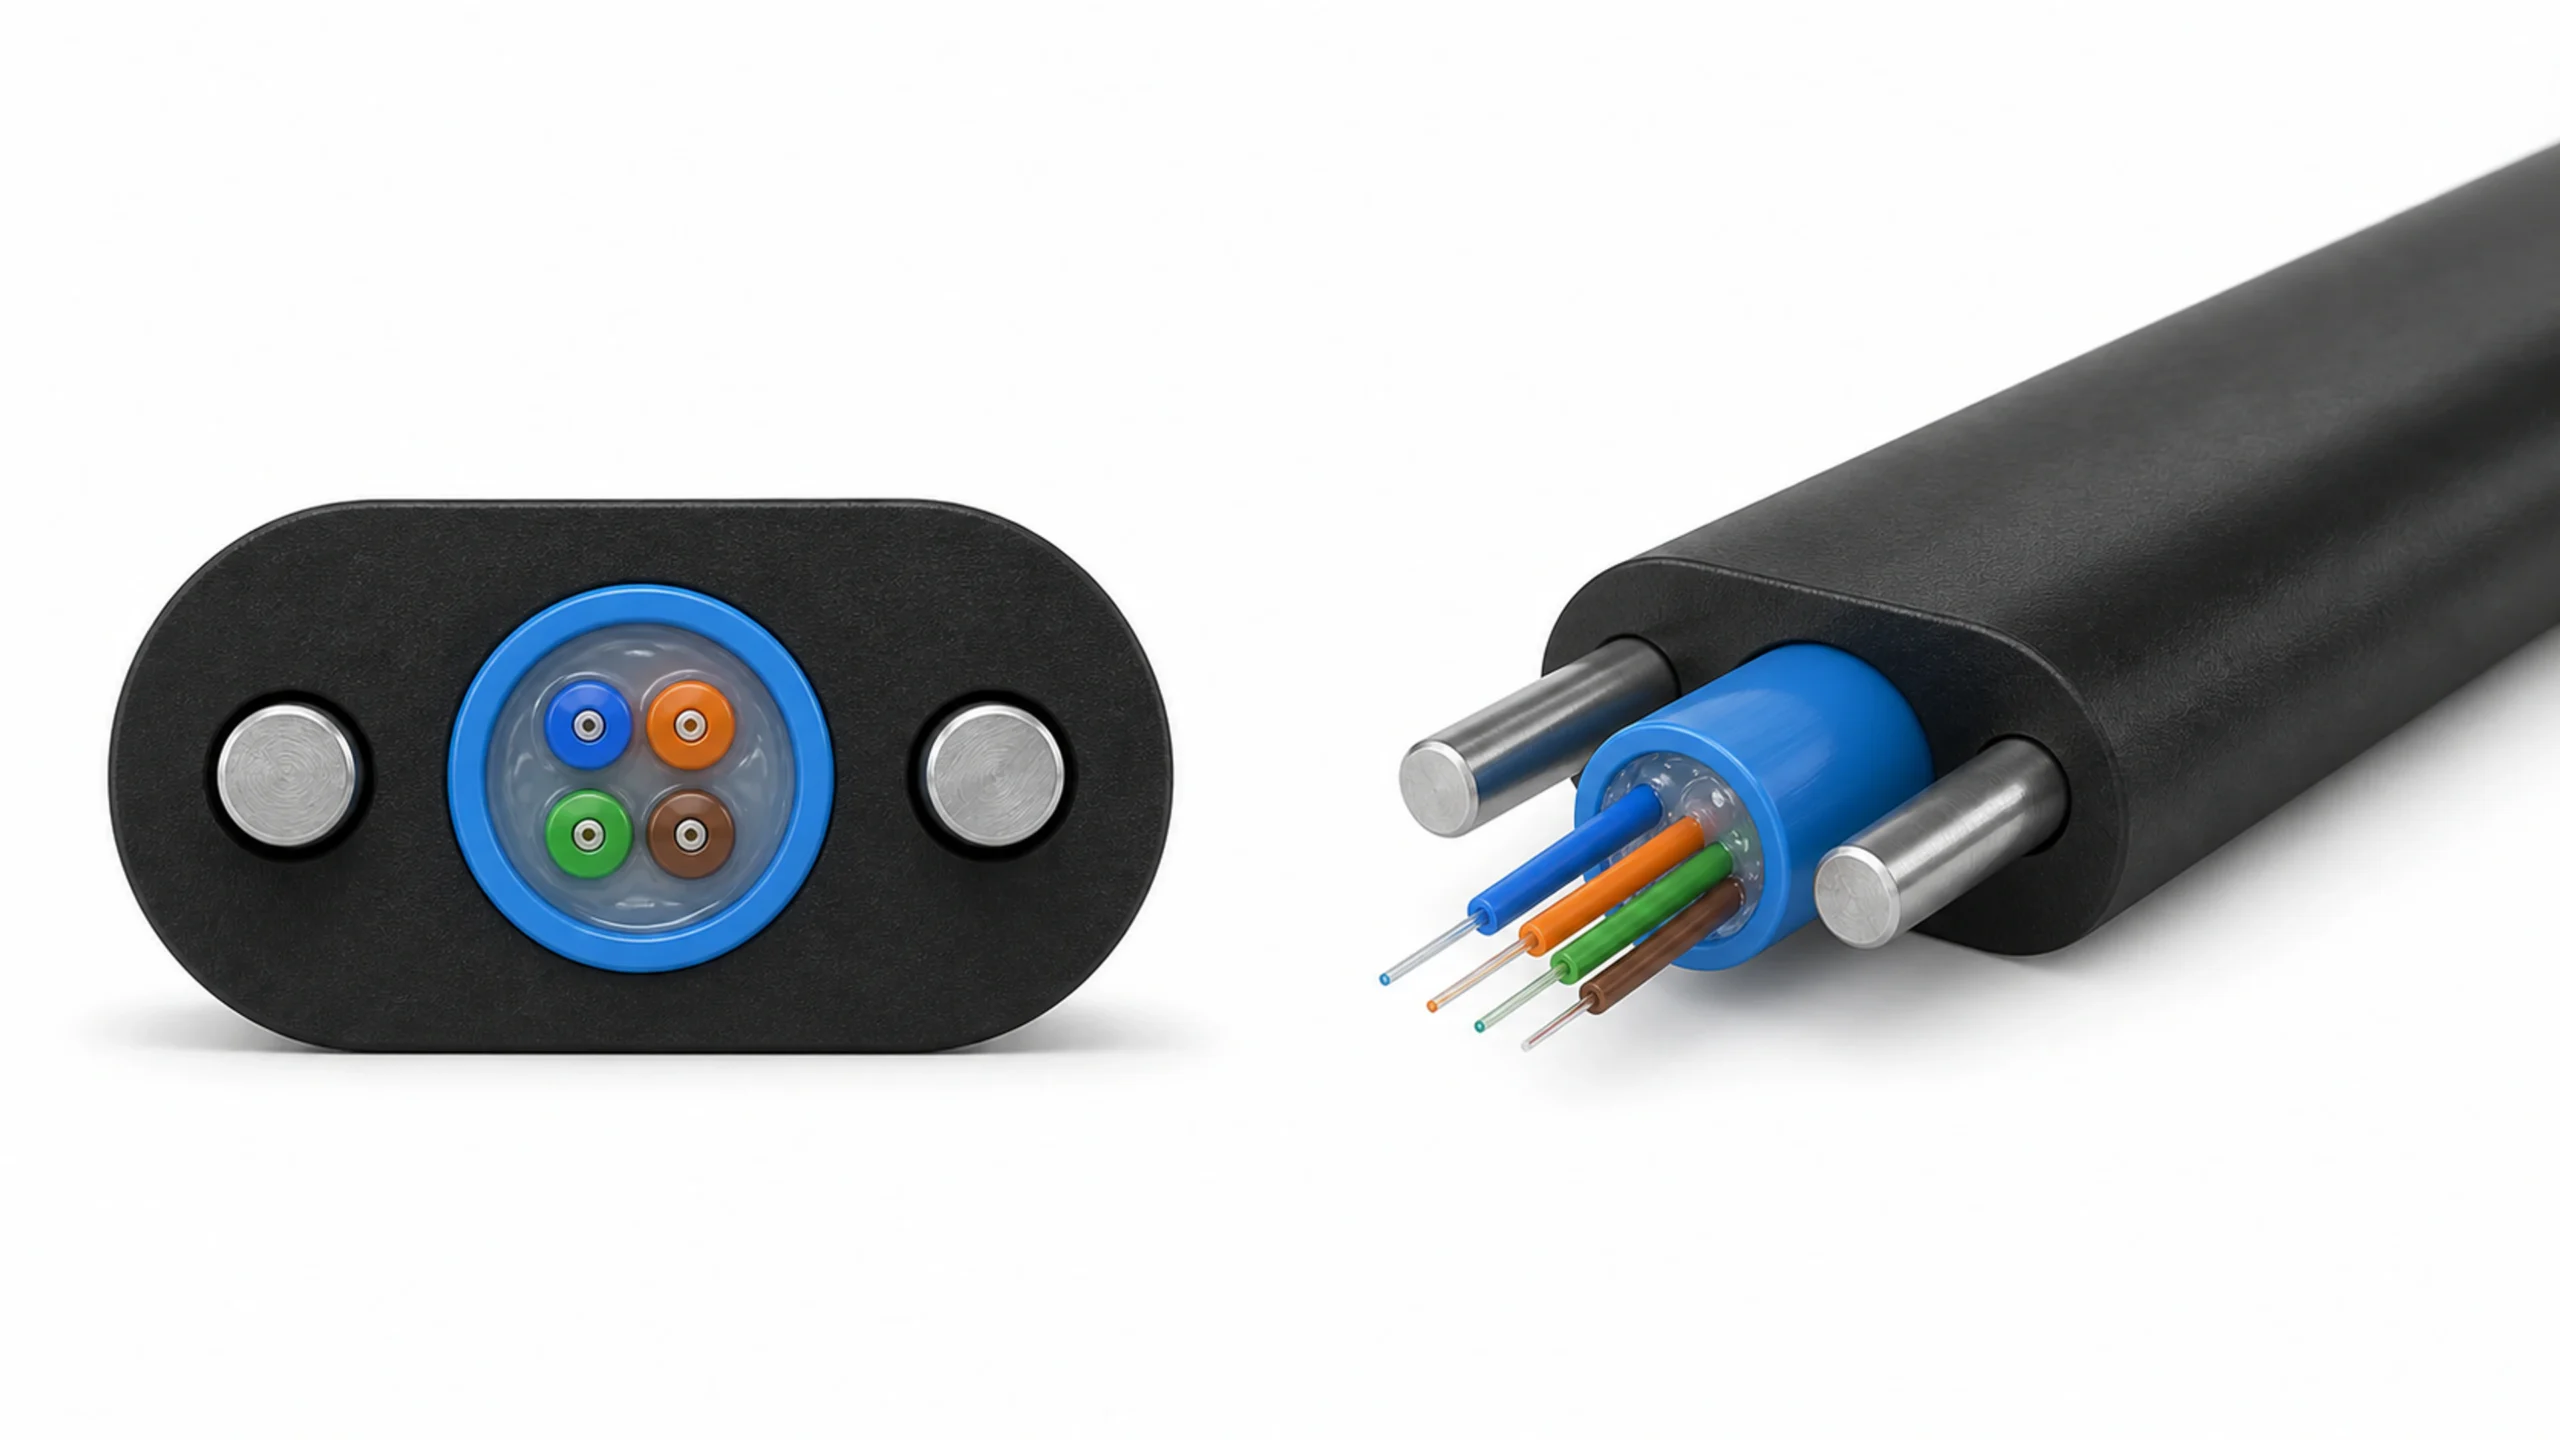
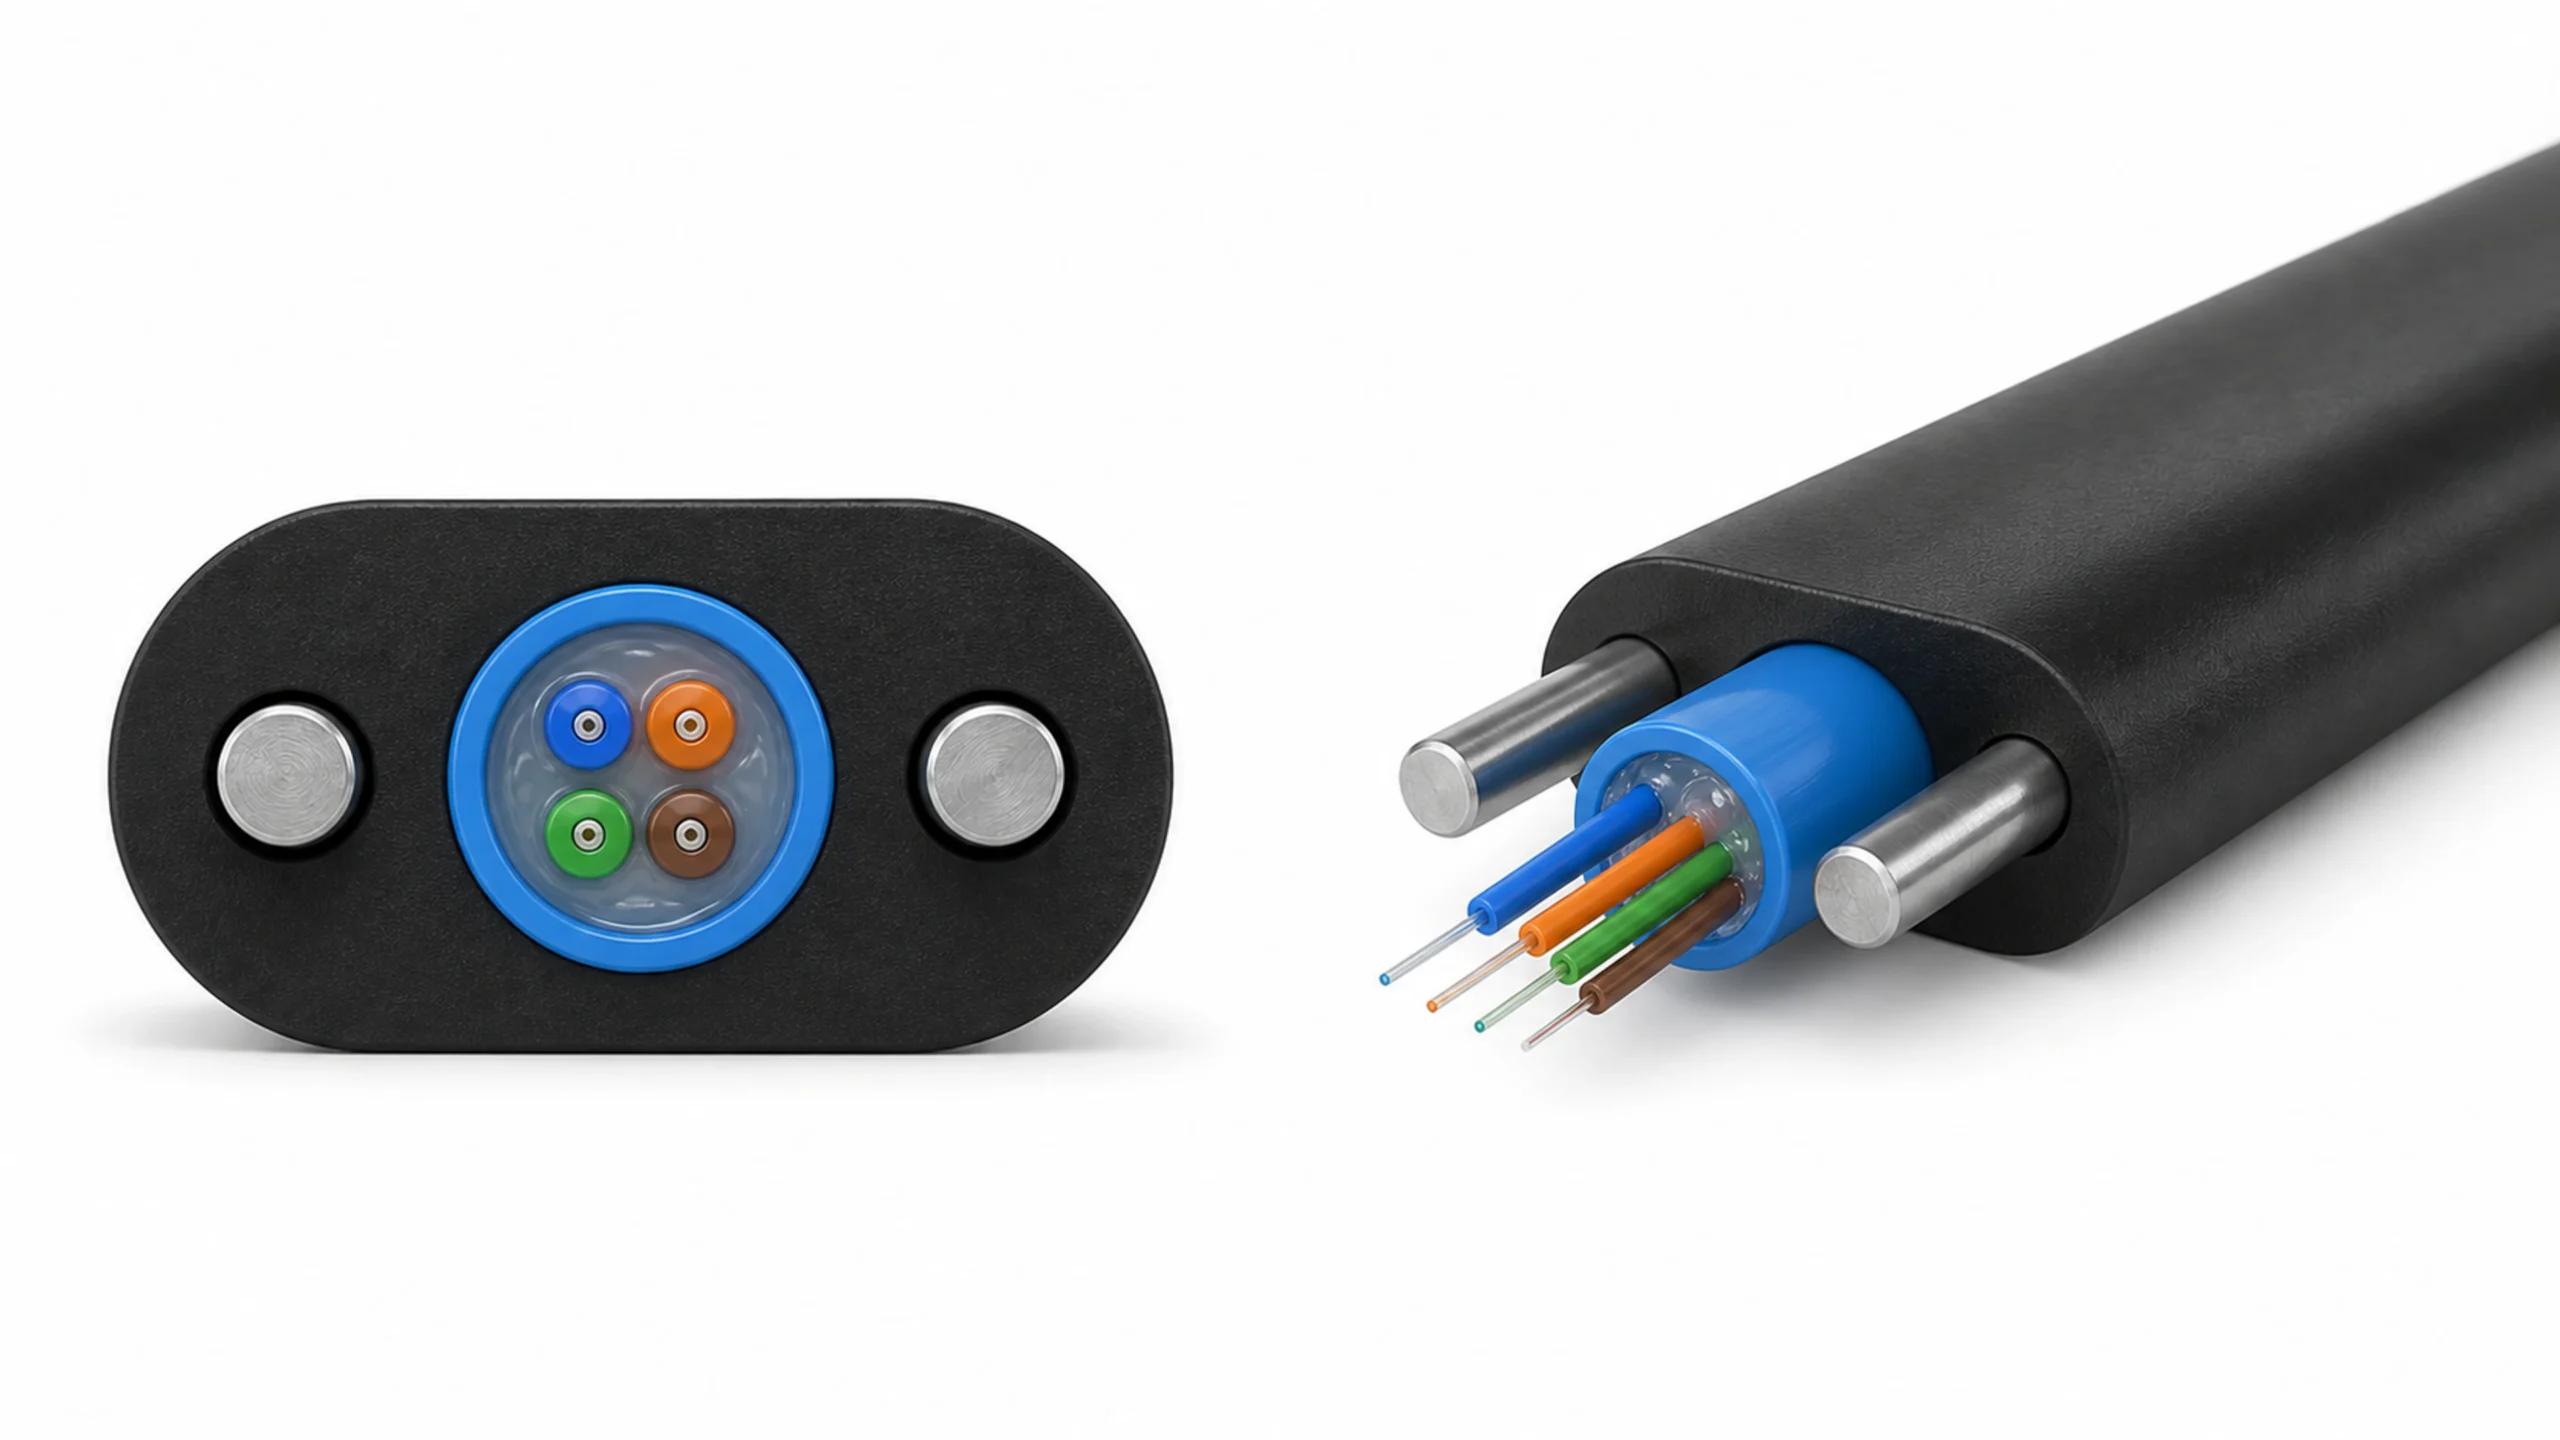

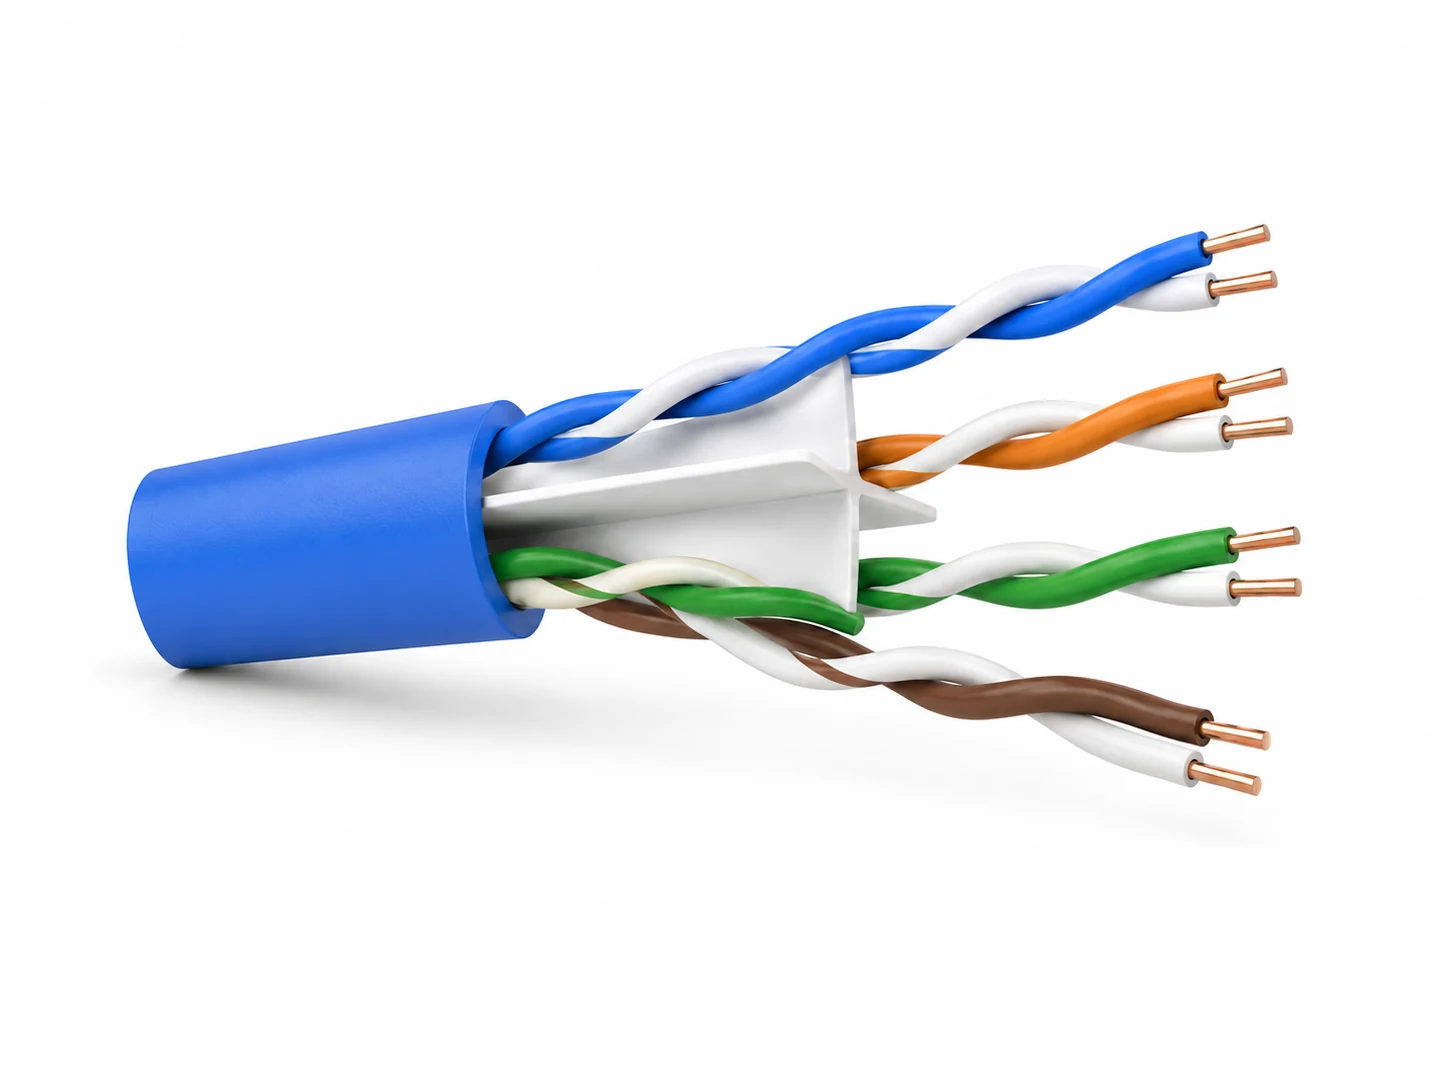


Cable structure preview
Reference cable
01
راهحل کابل انتخابشده
خط تولید کابل انعطافپذیر
What is a flexible cable production line? It turns fine-stranded copper conductors into separately insulated cores, lays up the cores and applies an outer sheath. Start from the material you already have, then confirm each stage through testing and packing.
- Cable designation
- RVV / H05VV-F review
- مواد هادی
- Copper reference · final material to confirm
- مسیر هادی
- Bunch → Insulate cores → Lay up → Sheath
- Final configuration
- Confirmed against the approved cable design
02 Cable definition
Define the Flexible Cable Before Selecting Equipment
This three-core reference separates the fine copper wires inside each conductor from the separately insulated cable cores. Confirm both counts, then define insulation, core assembly and the outer sheath.

Known inputs and open confirmations
- خانواده کابل
- Unshielded multi-core Flexible Cable
- Reference designations
- RVV / H05VV-F family review; not interchangeable approvals
- مواد هادی
- Fine-stranded copper in this reference; grade and class to confirm
- Individual-wire diameter d
- Diameter of each copper wire, in mm · To be confirmed
- Copper wires per conductor n
- Number of wires in each bare conductor · To be confirmed
- Bare-conductor diameter / area
- Finished bare OD and nominal mm² · To be confirmed
- Insulated cable cores N
- Three-core artwork; project core count and identification to confirm
- عایق هسته
- PVC example; compound, wall thickness and insulated-core OD to confirm
- Core laying-up
- Lay length, direction and laid-up bundle OD to confirm
- Fillers / binder
- فقط در مواردی که در ساخت تأییدشده مشخص شده است
- پوسته خارجی
- PVC example; grade, wall thickness and finished-cable OD to confirm
- Rated voltage / designation
- Product-specific standard and application · To be confirmed
- Output / finished package
- Cable size, quantity, working hours and coil or reel · To be confirmed
- پایه پذیرش
- Approved drawing and specified finished-cable tests · To be confirmed
Strand count is not the number of insulated cable cores.
Specify each conductor as n × d mm: n is the copper-wire count and d is the individual-wire diameter. Specify N separately as the number of insulated cores in the finished cable. Bunch the copper wires before insulation; lay up the insulated cores before outer sheathing.
03 Preliminary process route
Match the Route to the Cable Construction
This route illustrates an unshielded, multi-core flexible cable with PVC core insulation and a PVC outer sheath. Start from individual copper wires, prepared flexible conductors or approved insulated cores; do not repeat work already completed.
Prepare fine wires if needed → Bunch conductors → Insulate and check cores → Lay up cores → Extrude sheath → Cool, inspect and take up
Copper-wire count n is per conductor. Core count N is per finished cable. Final tests and packing follow the approved product specification.
Typical process / not a fixed layout
Read the order, not a fixed machine spacing: bunching forms each bare conductor; cabling lays up separately insulated cores. Cool, dry and check the cores before cabling. Sheathing has its own cooling, haul-off and take-up. Feed systems stay within the relevant line; no separate pay-off process stage is added. Intermediate reels and changeovers depend on the approved layout.

Stage 02 / Before core insulation
Fine-Wire Bunching
Form multiple fine copper wires into one flexible bare conductor before insulation.
- ورودی
- Copper wires per conductor n × individual-wire diameter d
- خروجی
- یک هادی انعطافپذیر روی یک قرقره میانی توافقشده
- Equipment source
- Equipment category; model, manufacturer and supply scope in the confirmed proposal
- Confirm
- Conductor class, wire count, wire diameter, lay, tension, bare OD and resistance; this is not insulated-core cabling
04 Equipment by required stage
Review the Equipment Categories for This Route
Review each machine’s actual function, then confirm its model and interfaces. These are 3D category references—not an automatic equipment configuration or a claim that one machine performs every downstream operation.
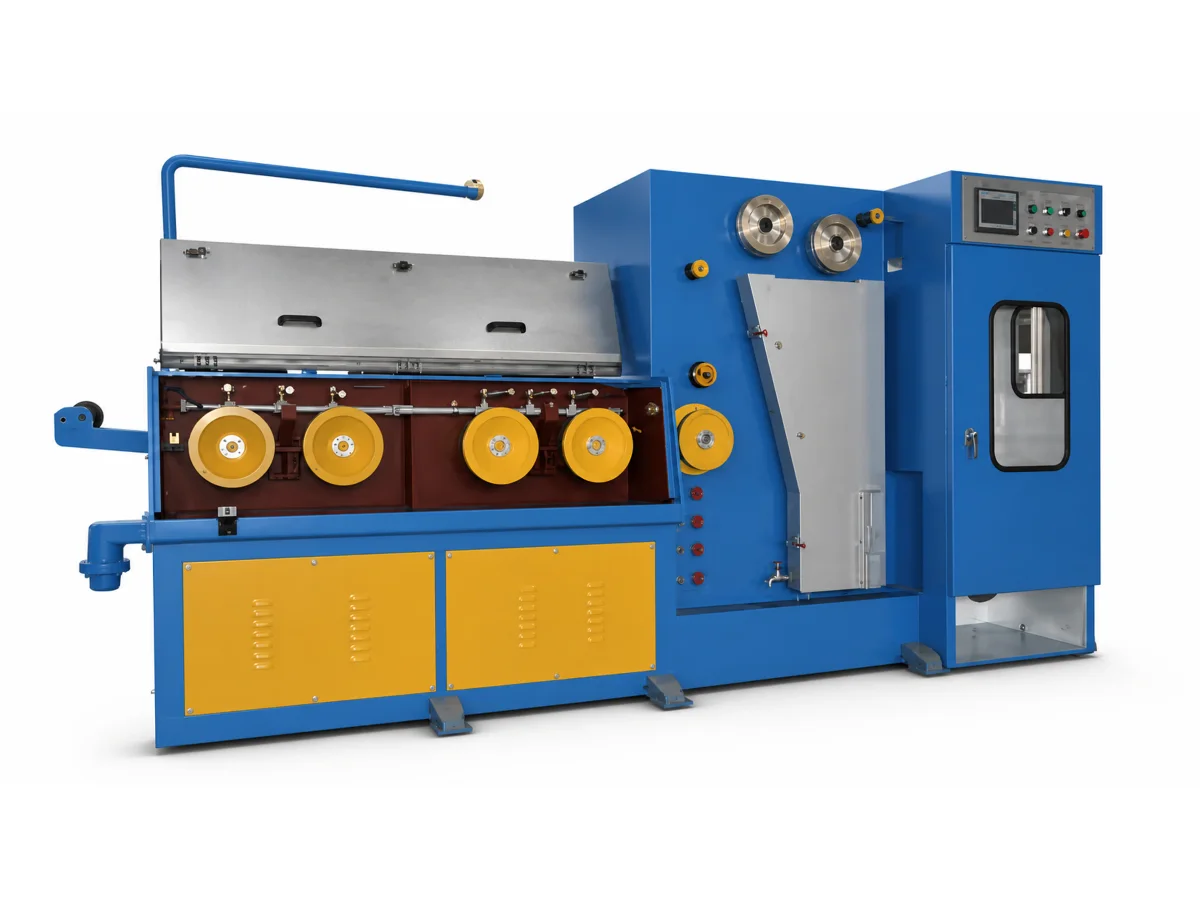 3D equipment reference · final model and configuration to confirm
01 / Equipment configuration
Fine-Wire Drawing / Annealing
Prepare fine-wire diameter and copper condition where the incoming material requires it.
Incoming and final wire diameter, annealing condition, spool format and resistance; do not repeat preparation on accepted incoming wire. The existing render represents a drawing-equipment family, not a verified fine-wire operating range.
07 Quality checkpoints
Check the Conductor, Insulation and Finished Cable
Agree the inspection plan before equipment selection. These 3D references explain the checks; they are not factory photographs, customer cases or evidence of passed tests.
Conductor acceptanceConductor acceptance
Check the Bare Conductor
Confirm wire count, individual-wire diameter, lay, finished bare-conductor diameter and the specified conductor resistance.
Wire count inside one conductor is not the number of insulated cores. The 3D cable is a structure illustration, not a test sample.
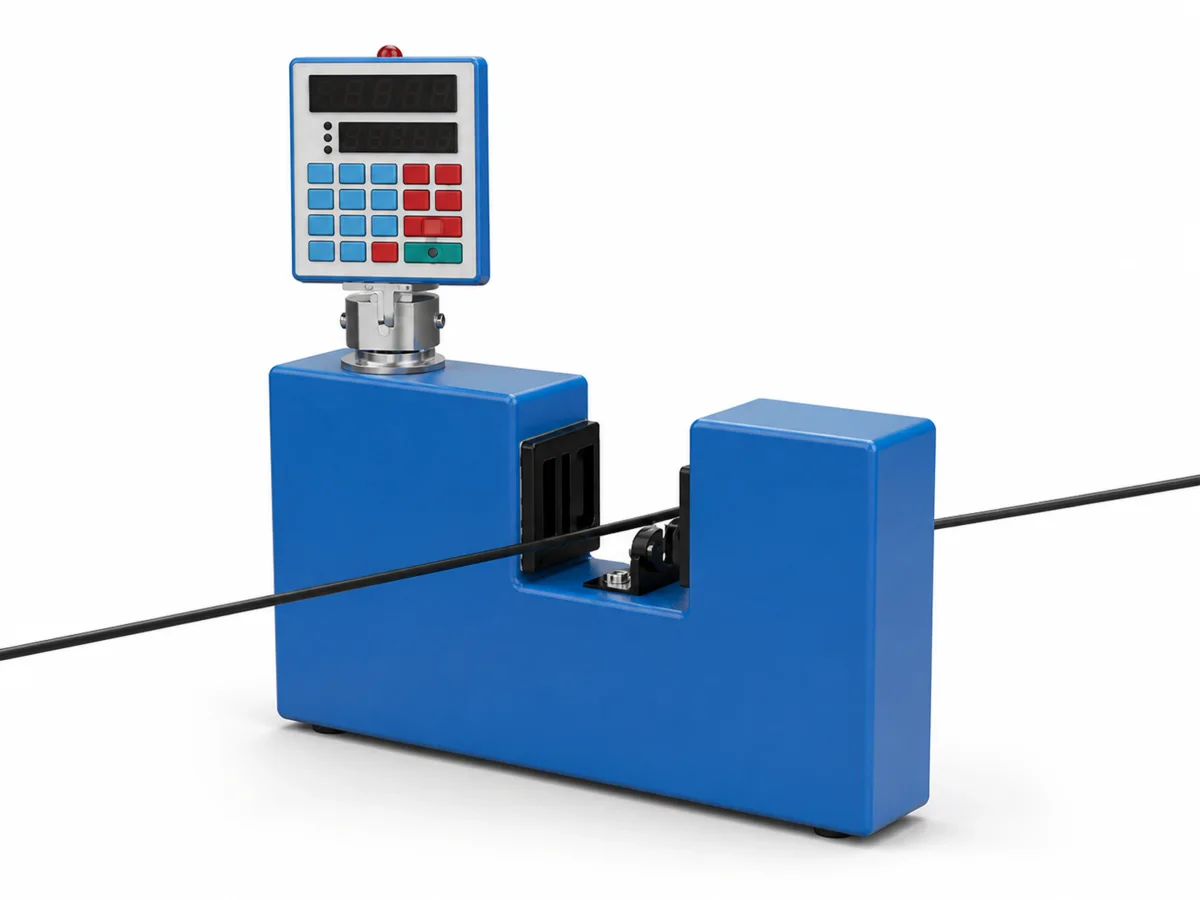 Dimensional control
Measure Diameter; Verify the Wall
Measure insulated-core and finished-cable diameters. Verify core insulation and outer-sheath wall thickness separately by the approved measurement method.
A laser outside-diameter gauge alone cannot establish minimum wall thickness. The acceptance method and tolerances must be defined.
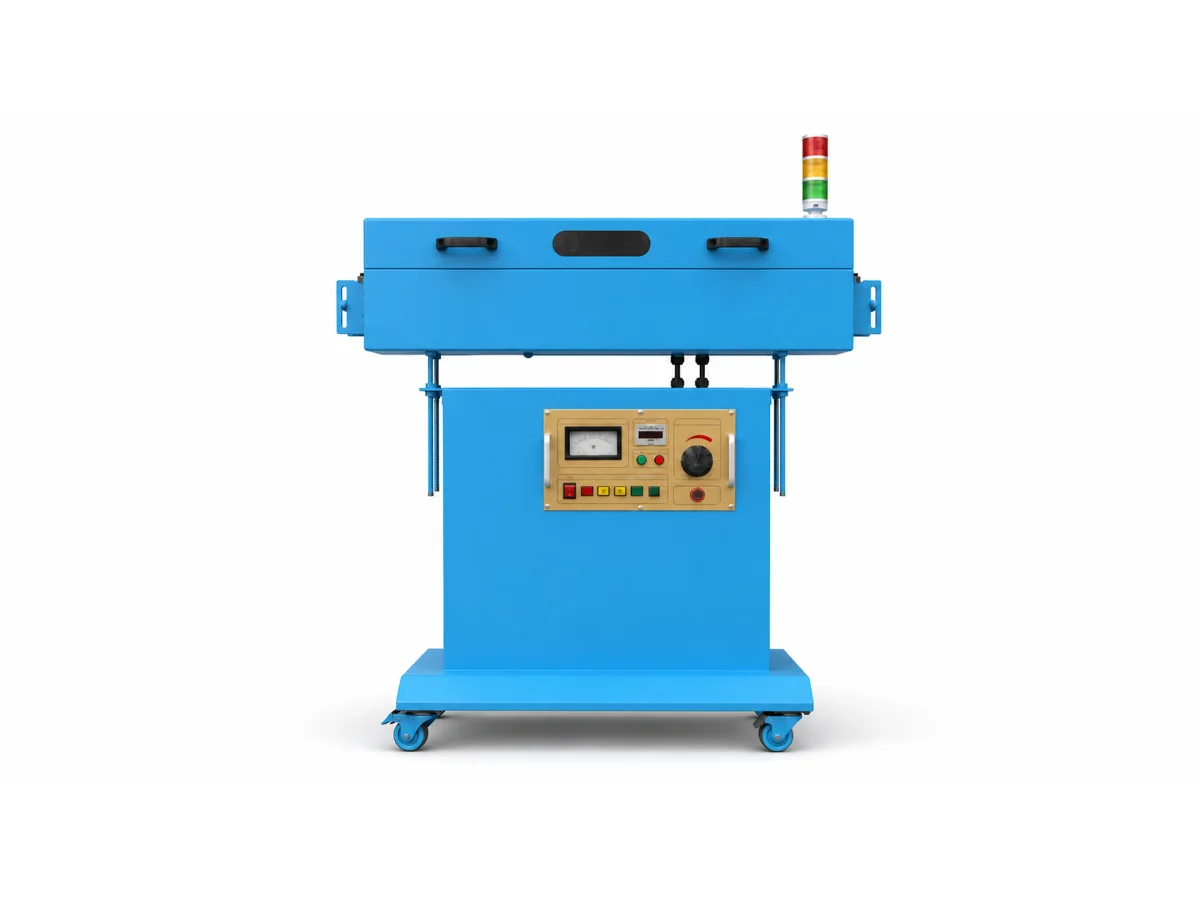 In-line electrical check
Inspect the Dry Insulation
Cool and dry each insulated core before its specified spark test. Record faults and keep accepted core reels identifiable before cabling.
Core spark testing does not replace finished-cable electrical tests. Any sheath integrity test needs its own approved method and suitable electrical arrangement.
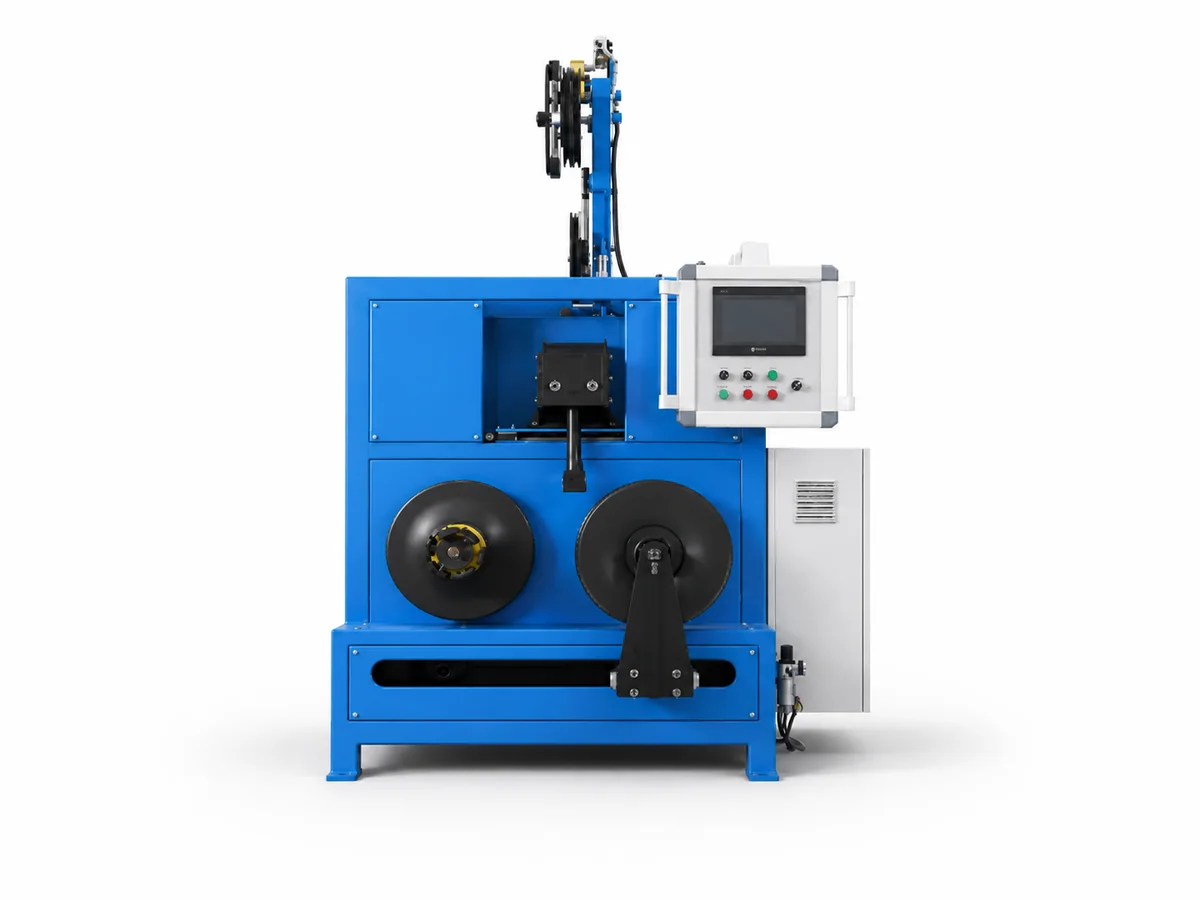 Finished-product release
Confirm the Sale-Ready Package
Verify core identification and continuity, conductor resistance, agreed electrical and material tests, cable dimensions, marking, length and packing before release.
The coiling-machine image illustrates handling only. Test records, product approval and FAT/SAT evidence require actual project data.
Keep illustration and evidence separate. Add actual trial records, sample measurements and project acceptance documents once available. No performance or certification is inferred from a render.
Project records required

