

UV-LAMP & LED CONFIGURATIONSUV-lamp machine — equipment image
UV-lamp equipment image from the outdoor cable project reference.
CONFIGURE THE WHOLE PROCESSFiber + ink + curing + tension + reel compatibility
Identify every fiber. Control every reel.
Apply and cure identification ink on individual optical fibers, then rewind them with coordinated tension and traverse. Select the curing system, fiber path and reel package around your production requirements.
UV-lamp equipment image from the outdoor cable project reference.
Fiber preparation: this machine colors or rewinds individual optical fibers. Loose-tube extrusion, tight buffering and cable sheathing are separate downstream processes.
Coloring follows all four steps. For rewinding without a new color coating, the machine uses the confirmed transfer path and operating settings.
Coordinate the driven pay-off, dancer and guide path with the actual supply reel.
Select the ink and die, center the coating system and set the required application conditions.
Match the UV-lamp or LED system, nitrogen protection and speed to the approved ink.
Coordinate wheel haul-off, winding tension and traverse for the required reel package.
Compare UV-lamp coloring, an LED configuration and rewinding mode. Each requires its own operating and acceptance conditions.
Select a unit to review its role and project requirements. These functions are integrated into the complete machine; the supplied reference image shows the whole equipment.
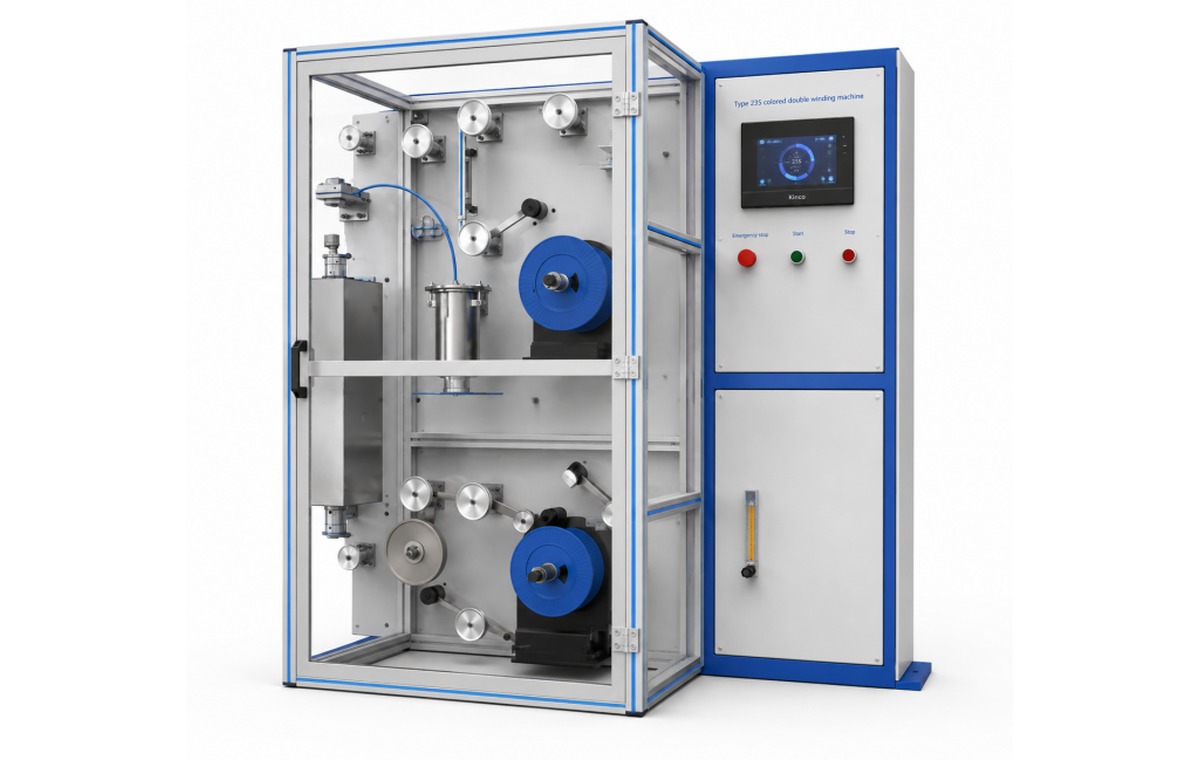
UV-lamp complete-machine image. Individual component photos and the final internal layout are confirmed for the selected project.
Feeds one optical fiber from the supply reel. The movable, motor-driven pay-off coordinates reel motion with fiber demand to limit tension variation and vibration.
Supply reel flange, barrel, bore, width and mass; fiber length; drive and threading arrangement.
Selected unit 01: Driven fiber pay-off
Select the complete UV-lamp or LED configuration. The electrical supply, drives, curing unit and speed ratings below belong to the stated reference equipment.
| Process | Single-fiber coloring and rewinding |
|---|---|
| Coloring production speed | Up to 1,800 m/min |
| Mechanical design speed | Up to 2,000 m/min |
| Rewinding speed | Confirm in the selected technical proposal |
| Curing technology | UV lamp with nitrogen flushing |
| UV lamp power | 7.5 kW |
| Color coating thickness | 3–5 μm |
| Pay-off tension | 0.2–1.0 N; tolerance ±0.05 N |
| Reel reference | 25 / 50 km classes; final reel dimensions to confirm |
| Pay-off drives | 2 × 1.5 kW Panasonic servos; 0.4 kW traverse |
| Wheel haul-off | 0.75 kW Panasonic servo |
| Take-up drives | 1.5 kW Panasonic servo; 0.4 kW traverse |
| Controls | Siemens S7 PLC; Kinco 10.2-inch HMI; RKC PID |
| Installed power reference | Approx. 13 kW |
| Electrical supply reference | 380 V / 50 Hz |
Reference configuration. Final supply, performance and utilities follow the agreed technical proposal and trial conditions.
| Process | Single-fiber coloring and rewinding |
|---|---|
| Coloring speed | 2,000 m/min |
| Mechanical design speed | 2,200 m/min |
| Rewinding speed | ≤2,200 m/min |
| Curing technology | LED oven with nitrogen protection |
| LED curing power | 3.7 kW |
| Cooling fan motor | 1.1 kW |
| Color coating thickness | 3–5 μm |
| Pay-off tension | 0.2–1.0 N; tolerance ±0.05 N |
| Traverse pitch | 0.1–2.0 mm |
| Additional attenuation after coloring | ≤0.02 dB/km; agreed test method and conditions |
| Maximum reel diameter / mass | Ø236 mm / 10 kg |
| Machine dimensions (L × W × H) | 1,900 × 1,350 × 2,100 mm |
| Pay-off drives | 2 × 1 kW Panasonic servos; 0.4 kW traverse |
| Wheel haul-off | 0.75 kW Panasonic servo |
| Take-up drives | 1 kW Panasonic servo; 0.4 kW traverse |
| Controls | Siemens S7-300 PLC; Kinco 10.2-inch HMI; RKC PID |
| Electrical supply reference | 440 V / 60 Hz |
| Nitrogen purity | ≥99.99% |
| Compressed air | 0.5 MPa |
| Operating ambient temperature | 20–25 °C |
| Coating die temperature | 20–60 °C; tolerance ±2 °C |
| Ink pressure / capacity | 0–2.0 bar / 2 kg |
Reference configuration. Final supply, performance and utilities follow the agreed technical proposal and trial conditions.
The LED unit's 3.7 kW curing rating is not total machine power. Confirm the installed-load schedule and agree the fiber, ink, cure, tension, winding and optical tests for the selected design.
The coloring machine prepares the fiber package. Select the downstream production stages from the finished cable drawing and the processes already available in your factory.
Feed the prepared fiber reels into the approved loose-tube extrusion and filling process.
Explore the routeConnect fiber preparation with loose tubes, stranded core, aramid reinforcement and sheathing.
Explore the routeStart from the finished cable to identify the required preparation and downstream equipment.
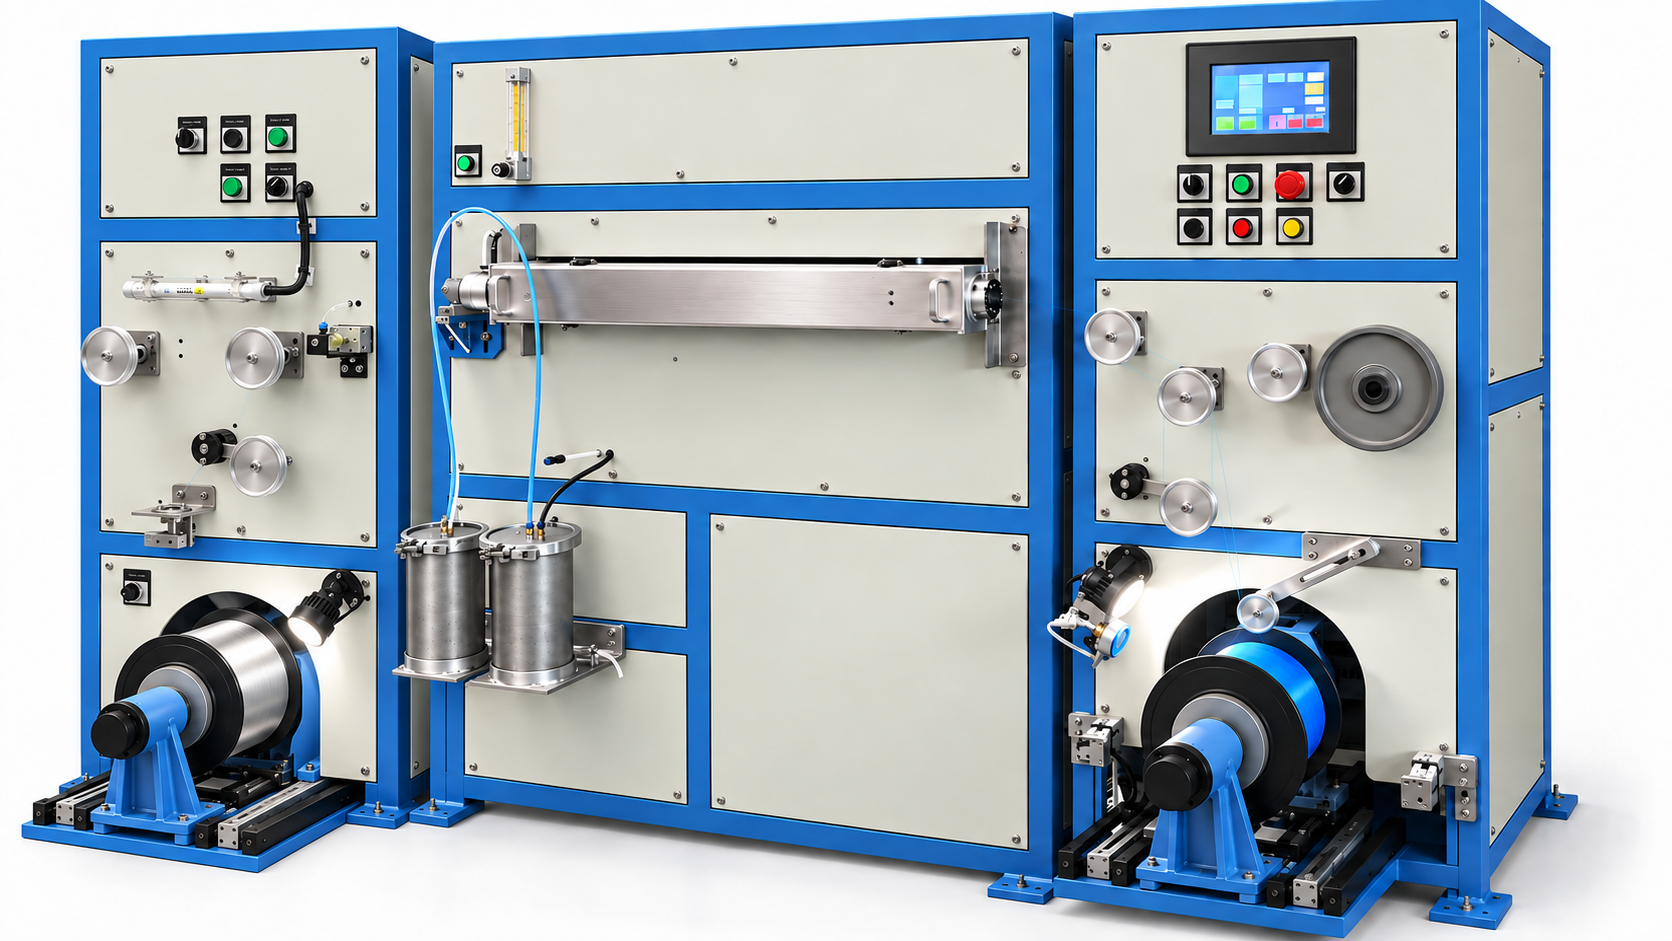
Explore the routeThe UV-lamp image and LED factory video show their respective equipment designs. Use the selected technical schedule and agreed trial conditions for acceptance.
Equipment image from the outdoor optical cable project. Review the lamp system, reel arrangement and final installation drawing with the UV-lamp specification.
View UV-lamp specifications →HONGKAI factory footage shows the fiber path, guide rollers, reel handling and HMI with a 2,000 m/min display. The display is an operating reference; acceptance uses the agreed materials and quality tests.
Confirm fiber condition, ink, input reel and output package before running the selected machine.
Check tension, coating, curing, haul-off and winding during starts, stable production and stops.
Record color identification, coating and cure quality, reel build and the agreed optical measurements.
The written proposal should connect equipment selection, integration and start-up responsibilities. Confirm the scope with HONGKAI for your project.
Start with your fiber, ink and reel specifications. Technical details can be confirmed during the first review.
Fiber type, coating diameter and incoming condition
Color program, ink brand / grade and coating target
UV-lamp or LED curing preference
Input and output reel drawings, mass and length
Target coloring and rewinding duties
Tension, winding and optical quality requirements
Site voltage, frequency, nitrogen and compressed air
Workshop space, installation and service access
Trial materials, inspection method and acceptance scope
Review the fiber, curing method, reel compatibility and information needed for a proposal.
The supplied machine reference processes one optical fiber at a time. Different identification colors are applied according to the production program; a 12-color program does not mean 12 simultaneous fiber paths.
Coloring adds identification ink and cures it before winding. Rewinding transfers an existing fiber package with controlled tension and traverse, without applying a new color coating. Confirm the threading path and operating settings for the selected machine.
HONGKAI source documents include a UV-lamp machine reference and a separate LED-curing configuration. Select the system together with the ink, nitrogen, cooling, electrical supply and required production duty. Final scope follows the technical proposal.
No. Mechanical design speed, coloring speed and rewinding speed describe different limits or duties. Achievable coloring performance depends on fiber, ink, coating thickness, cure conditions, tension and the agreed quality criteria.
Reel length alone is insufficient. Provide flange and barrel diameters, width, bore, full-reel mass and winding requirements. The UV and LED source configurations have different stated reel references, so compatibility must be checked.
They are seven integrated functional units of the coloring and rewinding machine. The supplied outdoor-project document provides one complete-machine image, not seven independent component photographs.
It prepares identified fiber packages before processes such as loose-tube extrusion or tight buffering. The next production stage depends on the finished cable and on whether suitable pre-colored fiber is already supplied.
Send the fiber and ink specifications, required coloring or rewinding duty, reel drawings, target output, curing preference and site utilities. Add inspection and acceptance requirements and any existing equipment interfaces.


